WO2012127752A1 - リング体把持治具及びスクロール圧縮装置 - Google Patents
リング体把持治具及びスクロール圧縮装置 Download PDFInfo
- Publication number
- WO2012127752A1 WO2012127752A1 PCT/JP2011/079466 JP2011079466W WO2012127752A1 WO 2012127752 A1 WO2012127752 A1 WO 2012127752A1 JP 2011079466 W JP2011079466 W JP 2011079466W WO 2012127752 A1 WO2012127752 A1 WO 2012127752A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- gripping
- ring body
- peripheral surface
- ring
- gripping jig
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C23/00—Combinations of two or more pumps, each being of rotary-piston or oscillating-piston type, specially adapted for elastic fluids; Pumping installations specially adapted for elastic fluids; Multi-stage pumps specially adapted for elastic fluids
- F04C23/02—Pumps characterised by combination with, or adaptation to, specific driving engines or motors
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C18/00—Rotary-piston pumps specially adapted for elastic fluids
- F04C18/02—Rotary-piston pumps specially adapted for elastic fluids of arcuate-engagement type, i.e. with circular translatory movement of co-operating members, each member having the same number of teeth or tooth-equivalents
- F04C18/0207—Rotary-piston pumps specially adapted for elastic fluids of arcuate-engagement type, i.e. with circular translatory movement of co-operating members, each member having the same number of teeth or tooth-equivalents both members having co-operating elements in spiral form
- F04C18/0215—Rotary-piston pumps specially adapted for elastic fluids of arcuate-engagement type, i.e. with circular translatory movement of co-operating members, each member having the same number of teeth or tooth-equivalents both members having co-operating elements in spiral form where only one member is moving
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C18/00—Rotary-piston pumps specially adapted for elastic fluids
- F04C18/02—Rotary-piston pumps specially adapted for elastic fluids of arcuate-engagement type, i.e. with circular translatory movement of co-operating members, each member having the same number of teeth or tooth-equivalents
- F04C18/0207—Rotary-piston pumps specially adapted for elastic fluids of arcuate-engagement type, i.e. with circular translatory movement of co-operating members, each member having the same number of teeth or tooth-equivalents both members having co-operating elements in spiral form
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C23/00—Combinations of two or more pumps, each being of rotary-piston or oscillating-piston type, specially adapted for elastic fluids; Pumping installations specially adapted for elastic fluids; Multi-stage pumps specially adapted for elastic fluids
- F04C23/008—Hermetic pumps
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C29/00—Component parts, details or accessories of pumps or pumping installations, not provided for in groups F04C18/00 - F04C28/00
- F04C29/0042—Driving elements, brakes, couplings, transmissions specially adapted for pumps
- F04C29/0078—Fixing rotors on shafts, e.g. by clamping together hub and shaft
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C29/00—Component parts, details or accessories of pumps or pumping installations, not provided for in groups F04C18/00 - F04C28/00
- F04C29/02—Lubrication; Lubricant separation
- F04C29/026—Lubricant separation
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C29/00—Component parts, details or accessories of pumps or pumping installations, not provided for in groups F04C18/00 - F04C28/00
- F04C29/02—Lubrication; Lubricant separation
- F04C29/028—Means for improving or restricting lubricant flow
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C29/00—Component parts, details or accessories of pumps or pumping installations, not provided for in groups F04C18/00 - F04C28/00
- F04C29/0042—Driving elements, brakes, couplings, transmissions specially adapted for pumps
- F04C29/0085—Prime movers
Definitions
- the present invention relates to a ring body gripping jig and a scroll compression device when machining a ring body.
- a stator is supported inside a casing via a spacer ring (see, for example, Patent Document 1).
- This spacer ring is generally a thin ring body made of steel, and the processing accuracy of the inner and outer peripheral surfaces is important. If the coaxiality of the inner and outer diameters cannot be ensured, the stator cannot be accurately supported inside the casing.
- the ring body is gripped by a chuck of a processing machine via a jig, and the outer peripheral surface processing (or inner peripheral surface processing) is performed. Then, the jig is unclamped, the inner ring surface machining (or outer circumferential surface machining) is performed by gripping the outer ring processed ring body with another jig on the chuck of the processing machine.
- the inner ring surface machining or outer circumferential surface machining
- an object of the present invention is to solve the problems of the conventional techniques described above, and when performing the outer peripheral surface processing and inner peripheral surface processing of the ring body, ensure the coaxiality of the inner diameter and the outer diameter, and improve the processing accuracy.
- An object of the present invention is to provide a ring body gripping jig and a scroll compression device that can be improved.
- the present invention is fixed to a chuck of a processing machine in a ring body gripping jig for gripping the ring body when machining the outer peripheral surface and / or inner peripheral surface of the ring body.
- a gripping mechanism having a gripping jig main body having a fixed surface and a claw member that protrudes from the gripping surface of the gripping jig main body when the inner peripheral surface of the ring body is processed and presses the end surface of the ring body from the outside at the tip.
- a fastened part to which a fastener for fastening a pressing plate that presses the end face of the ring body toward the gripping surface of the gripping jig body at the time of processing the outer peripheral surface of the ring body is provided.
- the gripping mechanism portion having a claw member that protrudes from the gripping surface of the gripping jig main body and presses the end surface of the ring body from the outside at the time of processing the inner peripheral surface of the ring body is provided.
- the ring body can be processed by gripping the link body by the mechanism portion, and the end surface of the ring body is pressed toward the gripping surface of the gripping jig body when the outer peripheral surface of the ring body is processed.
- the gripping mechanism portion may include a claw member and a bolt for connecting the claw member to the gripping jig main body, and a female screw hole corresponding to the bolt may be formed on the gripping surface of the gripping jig main body.
- a recess in which the tip of the claw member can be fitted may be formed in the outer peripheral portion of the pressing plate.
- the gripping jig main body may be configured to be able to switch between gripping by the gripping mechanism unit and gripping by the pressing plate while gripping the ring body. In this configuration, the ring body is gripped by the gripping jig body via the gripping mechanism portion to perform inner peripheral surface processing, and then the gripping mechanism portion is gripped without being unclamped.
- the ring body may be configured to be switchable from the inner peripheral surface processing to the outer peripheral surface processing or from the outer peripheral surface processing to the inner peripheral surface processing while the ring body is held by the gripping jig body. In this configuration, it is possible to switch from inner surface processing to outer surface processing or from outer surface processing to inner surface processing while holding the ring body without unclamping. There is no correction, and the coaxiality of the inner and outer diameters can be secured.
- the present invention accommodates a scroll compression mechanism that compresses refrigerant in the casing, and a drive motor that is connected to the scroll compression mechanism by a drive shaft and drives the scroll compression mechanism.
- the scroll compression mechanism is supported on the casing by a main frame, the drive shaft is coupled to a rotor of the drive motor, the drive shaft is supported on the casing by a bearing plate, and the stator of the motor is defined in claims 1 to 5. After being formed by using the ring body gripping jig according to any one of claims 5 to 5, the ring body is supported by the casing.
- the ring body can be processed by gripping the link body by the gripping mechanism portion, and the end surface of the ring body can be attached via the presser plate by fastening the fastener to the fastened portion. It is possible to press the outer peripheral surface of the ring body in this state. Therefore, the coaxiality of the inner diameter and the outer diameter can be secured, and processing can be performed with high accuracy.
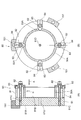
- FIG. 3 A is a sectional view showing a ring body gripping jig corresponding to FIG. 3, and B is a front view thereof.
- A is a sectional view showing a ring body gripping jig corresponding to FIG. 4, and B is a front view of the same.
- FIG. 1 shows a scroll compressor.
- Reference numeral 1 denotes a scroll compressor having an internal high pressure.
- the compressor 1 is connected to a refrigerant circuit (not shown) that performs a refrigeration cycle operation by circulating the refrigerant, and compresses the refrigerant.
- the compressor 1 has a vertically long cylindrical hermetic dome-shaped casing 3.
- the casing 3 includes a casing main body 5 that is a cylindrical body having an axis extending in the vertical direction, and a bowl-shaped upper cap having a convex surface that is welded and integrally joined to the upper end of the casing body 5 7 and a flange-like lower cap 9 which is welded and integrally joined to the lower end portion of the casing body 5 and has a convex surface protruding downward, and is configured as a pressure vessel.
- a terminal cover 52 is provided on the outer peripheral surface of the casing 3, and a power supply terminal 53 that supplies power to a stator 37 described later is provided inside the terminal cover 52.
- the casing 3 accommodates a scroll compression mechanism 11 that compresses the refrigerant and a drive motor 13 that is disposed below the scroll compression mechanism 11.
- the scroll compression mechanism 11 and the drive motor 13 are connected to each other by a drive shaft 15 disposed so as to extend in the vertical direction in the casing 3.
- a gap space 17 is formed between the scroll compression mechanism 11 and the drive motor 13.
- a main frame 21 is accommodated in the upper part of the casing 3, and a radial bearing portion 28 and a boss accommodating portion 26 are formed at the center of the main frame 21.
- the radial bearing portion 28 is for supporting the tip (upper end) side of the drive shaft 15 and is formed to project downward from the center of one surface (lower surface) of the main frame 21. .
- the boss accommodating portion 26 is for accommodating a boss 25C of the swing scroll 25 described later, and is formed by recessing the center of the other surface (upper surface) of the main frame 21 downward.
- An eccentric shaft portion 15 ⁇ / b> A is formed at the tip (upper end) of the drive shaft 15.
- the eccentric shaft portion 15 ⁇ / b> A is provided with its center being eccentric from the axis of the drive shaft 15, and is inserted into the boss 25 ⁇ / b> C via the swing bearing 24 so as to be capable of being driven to rotate.
- the scroll compression mechanism 11 includes a fixed scroll 23 and a swing scroll 25.
- the fixed scroll 23 is disposed in close contact with the upper surface of the main frame 21.
- the main frame 21 is attached to the inner surface of the casing body 5, and the fixed scroll 23 is fastened and fixed to the main frame 21 with screws 34.
- the swing scroll 25 meshes with the fixed scroll 23 and is disposed in the swing space 12 formed between the fixed scroll 23 and the main frame 21.
- the casing 3 is partitioned into a high-pressure space 27 below the main frame 21 and a discharge space 29 above the main frame 21.
- the spaces 27 and 29 communicate with each other through vertical grooves 71 formed to extend vertically on the outer periphery of the main frame 21 and the fixed scroll 23.
- the upper cap 7 of the casing 3 has a suction pipe 31 that guides the refrigerant in the refrigerant circuit to the scroll compression mechanism 11, and the casing body 5 has a discharge pipe 33 that discharges the refrigerant in the casing 3 to the outside of the casing 3. It is fixed in a penetrating manner.
- the suction pipe 31 extends vertically in the discharge space 29, and an inner end thereof passes through the fixed scroll 23 of the scroll compression mechanism 11 and communicates with the compression chamber 35, and the refrigerant is introduced into the compression chamber 35 by the suction pipe 31. Is inhaled.
- the drive motor (DC drive motor) 13 is a DC (Direct Current) motor that is driven by receiving an input from a direct current power source, and includes an annular stator 37 and a rotor 39 that is configured to be rotatable inside the stator 37. Is provided.
- the drive motor 13 receives a constant input voltage, and its rotational torque is controlled by a PWM (Pulse Width Modulation) inverter that controls the duty ratio of the pulse wave, that is, the period for outputting the pulse wave and the pulse width when the pulse wave is output.
- PWM Pulse Width Modulation
- the swing scroll 25 of the scroll compression mechanism 11 is drivingly connected to the rotor 39 via the drive shaft 15.
- the stator 37 includes a stator core 37 ⁇ / b> A and the stator coil 18.
- the stator core 37A is formed by stacking thin iron plates, and has a plurality of grooves inside although not shown.
- the stator coil 18 is formed by winding a plurality of phases of stator windings, and is fitted into a groove formed inside the stator core 37A, and is provided above and below the stator core 37A.
- the stator coil 18 is accommodated in the insulator 19.
- the stator coil 18 is connected to the power supply terminal 53 via a lead wire (not shown).
- the rotor 39 is formed of a ferrite magnet or a neodymium magnet and is magnetized by magnetization.
- winding magnetization is performed by passing a current through a stator winding forming the stator coil 18 of the stator 37 and magnetizing the rotor 39.
- There is external magnetization that is inserted into the stator 37 after being magnetized using an external magnetizing device.
- a holder (pin holder) 58 used for positioning the rotor 39 when the rotor 39 is magnetized by winding is press-fitted inside the drive shaft 15.
- the stator 37 is supported on the inner wall surface of the casing 3 by an annular spacer ring 38.
- the spacer ring 38 is fixed to the inner wall surface of the casing 3 by shrink fitting, and the stator 37 is fixed to the inner wall surface of the spacer ring 38 by shrink fitting.
- the upper end surface of the spacer ring 38 is provided below the upper end surface of the stator 37.
- the bearing plate 8 that rotatably fits and supports the lower end portion of the drive shaft 15.
- the bearing plate 8 is formed in a cylindrical shape with a boss portion 8A into which the drive shaft 15 is inserted, and an arm portion 8B that is provided around the boss portion 8A at substantially equal intervals and extends in four directions and is fixed to the casing body 5. Is provided. That is, the drive shaft 15 is supported on the casing 3 by the bearing plate 8.
- the bearing plate 8 is formed between the arm portions 8B and has an opening 8E that communicates the upper and lower spaces.
- the baffle plate 14 is made of, for example, a thin plate-shaped punching metal having a large number of pores 14D.
- An oil supply passage 41 as a part of the high pressure oil supply means is formed in the drive shaft 15, and this oil supply passage 41 extends vertically inside the drive shaft 15 and enters an oil chamber 43 on the back surface of the swing scroll 25. Communicate.
- the oil supply path 41 is connected to an oil pickup 45 provided at the lower end of the drive shaft 15.
- a lateral hole 57 extending in the radial direction of the drive shaft 15 and penetrating the oil supply passage 41 is provided on the back side of the oil pickup 45.
- the holder 58 described above is press-fitted into the horizontal hole 57.
- the oil pickup 45 is press-fitted into the drive shaft 15 after the rotor 39 is magnetized.
- the oil pickup 45 includes a suction port 42 provided at the lower end and a paddle 44 formed above the suction port 42.
- the lower end of the oil pickup 45 is immersed in the lubricating oil stored in the oil sump 40, and the suction port 42 of the oil supply path 41 is opened in the lubricating oil.
- the lubricating oil stored in the oil sump 40 enters the oil supply passage 41 from the suction port 42 of the oil pickup 45 and is pumped upward along the paddle 44 of the oil supply passage 41.
- the pumped lubricating oil is supplied to the sliding portions of the scroll compression mechanism 11 such as the radial bearing 28 and the orbiting bearing 24 through the oil supply passage 41.
- the lubricating oil is supplied to the oil chamber 43 on the back of the orbiting scroll 25 through the oil supply passage 41, and is supplied from the oil chamber 43 to the compression chamber 35 through the communication path 51 provided in the orbiting scroll 25.
- the main frame 21 is formed with a return oil passage 47 that penetrates the main frame 21 in the radial direction from the boss accommodating portion 26 and opens into the vertical groove 71.
- a return oil passage 47 that penetrates the main frame 21 in the radial direction from the boss accommodating portion 26 and opens into the vertical groove 71.
- An oil collector 46 is provided below the return oil passage 47, and the oil collector 46 extends to the vicinity of the upper end of the spacer ring 38.
- a plurality of notches 54 are formed on the outer peripheral surface of the stator 37 so as to extend up and down the stator 37.
- Lubricating oil returned from the oil supply passage 41 through the return oil passage 47 and the oil collector 46 is returned to the oil sump 40 through the notches 54 and between the arm portions 8B of the bearing plate 8.
- the discharge pipe 33 is shown by a broken line for convenience of explanation, but the discharge pipe 33 is arranged out of phase with the oil collector 46.
- the fixed scroll 23 is composed of an end plate 23A and a spiral (involute) wrap 23B formed on the lower surface of the end plate 23A.
- the orbiting scroll 25 is composed of an end plate 25A and a spiral (involute) wrap 25B formed on the upper surface of the end plate 25A.
- the wrap 23B of the fixed scroll 23 and the wrap 25B of the swing scroll 25 are meshed with each other, so that a plurality of compression is performed between the fixed scroll 23 and the swing scroll 25 by the both wraps 23B and 25B.
- a chamber 35 is formed.
- the orbiting scroll 25 is supported by the fixed scroll 23 via the Oldham ring 61, and a bottomed cylindrical boss 25C projects from the center of the lower surface of the end plate 25A.
- an eccentric shaft portion 15 ⁇ / b> A is provided at the upper end of the drive shaft 15, and the eccentric shaft portion 15 ⁇ / b> A is rotatably fitted to a boss 25 ⁇ / b> C of the swing scroll 25.
- the drive shaft 15 is provided with a counterweight portion (upper balancer) 63 below the main frame 21, and a lower balancer 77 is provided below the rotor 39.
- the drive shaft 15 is dynamically balanced with the orbiting scroll 25, the eccentric shaft portion 15A, and the like by the upper balancer 63 and the lower balancer 77.
- the swinging scroll 25 is revolved by rotating the drive shaft 15 while balancing the weight by the upper balancer 63 and the lower balancer 77.
- the compression chamber 35 is configured to compress the refrigerant sucked from the suction pipe 31 as the volume between the wraps 23B and 25B contracts toward the center.
- a lower plate of the lower balancer 77 is provided with a rotor 39 and a regulation plate 55 that is caulked together with the lower balancer 77.
- the restriction plate 55 restricts the rotation of the rotor 39 when the rotor 39 is wound and magnetized.
- a cup 48 is fixed to the lower side of the main frame 21 with bolts 49 so as to surround the upper balancer 63.
- the cup 48 prevents the lubricating oil leaking from the clearance between the main frame 21 and the drive shaft 15 from being scattered to the discharge pipe side by the rotation of the upper balancer 63.
- a discharge hole 73 is provided in the central portion of the fixed scroll 23, and the gas refrigerant discharged from the discharge hole 73 is discharged to the discharge space 29 through the discharge valve 75, and the main frame 21 and the fixed scroll 23.
- the refrigerant flows out into the high-pressure space 27 below the main frame 21 through the vertical grooves 71 provided on the outer circumferences, and the high-pressure refrigerant is discharged out of the casing 3 through the discharge pipe 33 provided in the casing body 5.
- the stator 37 is supported on the inner wall surface of the casing 3 by the annular spacer ring 38.
- the spacer ring 38 is fixed to the inner wall surface of the casing 3 by shrink fitting, and the stator 37 is fixed to the inner wall surface of the spacer ring 38 by shrink fitting.
- the spacer ring 38 is a thin ring body 38A (see FIGS. 5 and 6).
- the ring body 38A is used by the same jig without unclamping.
- the inner peripheral surface can be processed by gripping.
- FIG. 2 shows the ring body gripping jig according to the present embodiment
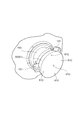
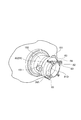
- FIG. 3 shows the ring body gripping jig when the inner peripheral surface of the ring body 38A is processed
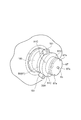
- FIG. 4 shows the outer peripheral surface processing of the ring body 38A.
- the ring body holding jig is shown.
- the ring body gripping jig 80 includes a solid disc-shaped gripping jig main body 81, and the gripping jig main body 81 is fixed to the chuck 151 of the processing machine 150.
- the chucks 151 are arranged at equal intervals of 120 ° in the circumferential direction, and move in the radial direction to grip the outer peripheral surface of the gripping jig body 81.
- FIG. 5 shows a ring body holding jig corresponding to FIG. 3 at the time of processing the inner peripheral surface of the ring body 38A.
- the gripping jig body 81 has a fixed surface 81A fixed to the chuck 151 of the processing machine, and the gripping surface 81B on the opposite side has an equal interval of 90 ° in the circumferential direction.
- four female screw holes 81C are formed.
- a bolt 82 is fastened to the female screw hole 81C so as to protrude from the gripping surface 81B, and a claw member 83 for holding the end face of the ring body 38A from the outside and a support pin 84 are disposed at the tip of the bolt 82.
- the support pin 84 is screwed into the outer end of the claw member 83 at the base end, and the tip end can freely contact the gripping surface 81B.
- the female screw hole 81C, the bolt 82, the claw member 83, the support pin 84, and the like constitute a gripping mechanism portion.
- This gripping mechanism portion is a gripping mechanism portion that is attached to the gripping surface 81B of the gripping jig body 81 when the inner peripheral surface of the ring body 38A is processed.
- the ring body 38A is first addressed to the gripping surface 81B of the gripping jig body 81 fixed to the chuck 151 of the processing machine, and the claw member 83 is disposed on the end surface of the ring body 38A.
- the bolt 82 is screwed in to press the end surface of the ring body 38 ⁇ / b> A, and the ring body 38 ⁇ / b> A is held between the gripping surface 81 ⁇ / b> B and the claw member 83.
- the ring body 38A is firmly held.
- the inner end of the claw member 83 is configured not to cover the inner diameter of the ring body 38A.
- FIG. 6 shows a ring body gripping jig at the time of processing the outer peripheral surface of the ring body 38A, corresponding to FIG.
- the gripping jig body 81 has a fixed surface 81A fixed to the chuck 151 of the processing machine, and has a female screw hole (fastened portion) at the center of the gripping surface 81B on the opposite side. 81D is formed.
- a bolt 85 is fastened to the female screw hole 81D, and the bolt 85 constitutes a fastener for stopping the pressing plate 87 that presses the end surface of the ring body 38A toward the gripping surface 81B of the gripping jig main body 81.
- the pressing plate 87 is a member for pressing the ring body 38A against the gripping surface 81B of the gripping jig main body 81 when processing the outer peripheral surface of the ring body 38A, and the outer diameter thereof is smaller than the outer diameter of the ring body 38A.
- Four semicircular arc-shaped recesses 87A are formed on the outer peripheral portion at equal intervals of 90 ° in the circumferential direction, and the distal end portion 83A of the claw member 83 can be freely fitted into the recess 87A as will be described later. It has become.
- the gripping mechanism main body 81 holds the ring body 38A and grips by the gripping mechanism, that is, as shown in FIG. As shown in FIG. 6, the gripping and the gripping by the pressing plate 87 can be switched.
- the inner diameter of the ring body 38A is first processed at the stage of finishing the spacer ring 38, and then the outer diameter is processed, first, as shown in FIG. 5, a female screw hole 81C, a bolt 82, a claw member 83, After holding the ring body 38A with the support pins 84 and the like and inserting the machining tool in the direction of arrow A, the tool is sent in the direction of arrow B to machine the inner peripheral surface of the ring body 38A.
- the holding plate 87 is finely adjusted so that the recess 87A faces the female screw hole 81C as shown in FIG.
- the claw member 83 is arranged so that the distal end portion 83A of the claw member 83 is positioned in the recess 87A on the outer peripheral portion of the pressing plate 87, and the claw member 83 is fastened by the bolt 82 to hold the ring body 38A.
- the gripping mechanism portion of FIG. 5 is removed, that is, the processing tool of the processing machine is moved in the direction of arrow A while keeping the gripping state shown in FIG. The tool is sent in the direction of arrow B to machine the outer peripheral surface.
- the present embodiment is configured to be able to switch between gripping by the gripping mechanism portion of FIG. 5 and gripping by the pressing plate 87 shown in FIG. 6 while gripping the ring body 38A on the gripping jig body 81.
- this invention is not limited to this.
- the manufacture of the spacer ring 38 in the scroll compressor has been described.
- the present invention is not limited to the spacer ring 38 and is suitable for manufacturing all thin-walled rings as general mechanical elements.
- the procedure from the inner peripheral surface processing in FIG. 5 to the outer peripheral surface processing in FIG. 6 has been described.
- the outer peripheral surface processing in FIG. 6 to the inner peripheral surface in FIG. Similarly, the coaxiality of the inner diameter and the outer diameter can be easily secured for the processing procedure.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Rotary Pumps (AREA)
- Applications Or Details Of Rotary Compressors (AREA)
Abstract
リング体の外周面加工や内周面加工を行う場合、加工精度を向上させることができるリング体把持治具を提供する。 リング体38Aの外周面および/または内周面を機械加工する際に当該リング体を把持するリング体把持治具80において、加工機のチャックに固定される固定面81Aを有した把持治具本体81と、前記リング体の内周面加工時に前記把持治具本体の把持面から突設され先端に当該リング体38Aの端面を外側から押さえる爪部材83を有した把持機構部と、前記リング体の外周面加工時に当該リング体の端面を前記把持治具本体の把持面81Bに向けて押圧する押さえ板を止める締結具が締結される被締結部81Dとを備えた。
Description
本発明は、リング体を機械加工する際のリング体把持治具及びスクロール圧縮装置に関する。
従来、例えばスクロール圧縮機などでは、そのケーシング内部にスペーサリングを介してステータを支持することが行われている(例えば、特許文献1参照)。
このスペーサリングは一般に鋼鉄製の薄肉のリング体であり、内周面および外周面の加工精度が重要であり、内径及び外径の同軸度を確保できないとケーシング内部にステータを精度良く支持できない。
このスペーサリングは一般に鋼鉄製の薄肉のリング体であり、内周面および外周面の加工精度が重要であり、内径及び外径の同軸度を確保できないとケーシング内部にステータを精度良く支持できない。
例えば、薄肉のリング体の外周面加工や内周面加工を行う場合、一般には、加工機のチャックにリング体を、治具を介して把持させ、外周面加工(あるいは内周面加工)を行い、ついで治具をアンクランプし、加工機のチャックに別の治具で外周面加工済みのリング体を把持し直して、内周面加工(あるいは外周面加工)を行っており、リング体の内径および外径の同軸度を確保し難い課題があった。
そこで、本発明の目的は、上述した従来の技術が有する課題を解消し、リング体の外周面加工や内周面加工を行う場合、内径および外径の同軸度を確保して、加工精度を向上できるリング体把持治具及びスクロール圧縮装置を提供することにある。
そこで、本発明の目的は、上述した従来の技術が有する課題を解消し、リング体の外周面加工や内周面加工を行う場合、内径および外径の同軸度を確保して、加工精度を向上できるリング体把持治具及びスクロール圧縮装置を提供することにある。
上記目的を達成するために、本発明は、リング体の外周面および/または内周面を機械加工する際に当該リング体を把持するリング体把持治具において、加工機のチャックに固定される固定面を有した把持治具本体と、前記リング体の内周面加工時に前記把持治具本体の把持面から突設され先端に当該リング体の端面を外側から押さえる爪部材を有した把持機構部と、前記リング体の外周面加工時に当該リング体の端面を前記把持治具本体の把持面に向けて押圧する押さえ板を止める締結具が締結される被締結部とを備えた、ことを特徴とする。
この発明では、前記リング体の内周面加工時に前記把持治具本体の把持面から突設され先端に当該リング体の端面を外側から押さえる爪部材を有した把持機構部を備えたため、該把持機構部でリンク体を把持して該リング体の内周面加工を行うことができ、前記リング体の外周面加工時に当該リング体の端面を前記把持治具本体の把持面に向けて押圧する押さえ板を止める締結具が締結される被締結部を備えたため、被締結部に締結具を締結することで、押さえ板を介してリング体の端面を押圧し、この状態でリング体の外周面加工を行うことができる。
この発明では、前記リング体の内周面加工時に前記把持治具本体の把持面から突設され先端に当該リング体の端面を外側から押さえる爪部材を有した把持機構部を備えたため、該把持機構部でリンク体を把持して該リング体の内周面加工を行うことができ、前記リング体の外周面加工時に当該リング体の端面を前記把持治具本体の把持面に向けて押圧する押さえ板を止める締結具が締結される被締結部を備えたため、被締結部に締結具を締結することで、押さえ板を介してリング体の端面を押圧し、この状態でリング体の外周面加工を行うことができる。
前記把持機構部が爪部材と当該爪部材を把持治具本体に連結するボルトとを備え、把持治具本体の把持面にボルトに対応した雌ねじ穴が形成されていてもよい。
前記押さえ板の外周部に爪部材の先端部が嵌合自在な凹所が形成されてもよい。
前記把持治具本体に前記リング体を把持したまま、前記把持機構部による把持と、前記押さえ板による把持とを切り替え可能に構成されていてもよい。
この構成では、前記把持治具本体に前記把持機構部を介して前記リング体を把持して内周面加工を行い、その後に、アンクランプせずに、前記把持機構部で把持したまま、前記把持機構部による把持から、前記押さえ板による把持へ切り替え、しかる後、前記把持機構部を撤去して、前記リング体の外周面加工を行うことができ、リング体の把持し直しがなくなり、内径および外径の同軸度を確保できる。
前記押さえ板の外周部に爪部材の先端部が嵌合自在な凹所が形成されてもよい。
前記把持治具本体に前記リング体を把持したまま、前記把持機構部による把持と、前記押さえ板による把持とを切り替え可能に構成されていてもよい。
この構成では、前記把持治具本体に前記把持機構部を介して前記リング体を把持して内周面加工を行い、その後に、アンクランプせずに、前記把持機構部で把持したまま、前記把持機構部による把持から、前記押さえ板による把持へ切り替え、しかる後、前記把持機構部を撤去して、前記リング体の外周面加工を行うことができ、リング体の把持し直しがなくなり、内径および外径の同軸度を確保できる。
前記把持治具本体に前記リング体を把持したまま、内周面加工から外周面加工へ、あるいは外周面加工から内周面加工へ切り替え可能に構成されていてもよい。
この構成では、アンクランプせずに、リング体を把持したまま、内周面加工から外周面加工へ、あるいは外周面加工から内周面加工へ切り替え可能に構成されるため、リング体の把持し直しがなくなり、内径および外径の同軸度を確保できる。
この構成では、アンクランプせずに、リング体を把持したまま、内周面加工から外周面加工へ、あるいは外周面加工から内周面加工へ切り替え可能に構成されるため、リング体の把持し直しがなくなり、内径および外径の同軸度を確保できる。
また、上記目的を達成するために、本発明は、ケーシングの内部に冷媒を圧縮するスクロール圧縮機構と、前記スクロール圧縮機構と駆動軸で連結され当該スクロール圧縮機構を駆動する駆動モータとが収容され、前記スクロール圧縮機構がメインフレームにより前記ケーシングに支持され、前記駆動モータのロータに前記駆動軸が連結され、当該駆動軸がベアリングプレートにより前記ケーシングに支持され、前記モータのステータは請求項1ないし5のいずれか一項に記載のリング体把持治具を利用して加工形成された後、前記ケーシングに支持されたことを特徴とする。
本発明では、把持機構部でリンク体を把持して該リング体の内周面加工を行うことができ、被締結部に締結具を締結することで、押さえ板を介してリング体の端面を押圧し、この状態でリング体の外周面加工を行うことができる。従って、内径、外径の同軸度を確保でき、精度よく加工できる。
以下、本発明の一実施の形態を図面に基づいて説明する。
図1は、スクロール圧縮装置を示す。
1は内部高圧となるスクロール圧縮装置であり、この圧縮機1は、冷媒が循環して冷凍サイクル運転動作を行う図外の冷媒回路に接続されて、冷媒を圧縮するものである。この圧縮機1は、縦長円筒状の密閉ドーム型のケーシング3を有する。
このケーシング3は、上下方向に延びる軸線を有する円筒状の胴部であるケーシング本体5と、その上端部に気密状に溶接されて一体接合され、上方に突出した凸面を有する椀状の上キャップ7と、ケーシング本体5の下端部に気密状に溶接されて一体接合され、下方に突出した凸面を有する椀状の下キャップ9とで圧力容器に構成されており、その内部は空洞とされている。ケーシング3の外周面には、ターミナルカバー52が設けられ、このターミナルカバー52の内部には、後述のステータ37に電源を供給する電源供給端子53が備えられる。
ケーシング3の内部には、冷媒を圧縮するスクロール圧縮機構11と、このスクロール圧縮機構11の下方に配置される駆動モータ13とが収容されている。これらのスクロール圧縮機構11と駆動モータ13とは、ケーシング3内を上下方向に延びるように配置される駆動軸15によって連結されている。
また、これらのスクロール圧縮機構11と駆動モータ13との間には間隙空間17が形成されている。
ケーシング3の内部上方には、メインフレーム21が収納され、このメインフレーム21には中央にラジアル軸受部28とボス収容部26とが形成されている。ラジアル軸受部28は、駆動軸15の先端(上端)側を軸支するためのものであり、当該メインフレーム21の一方の面(下側の面)の中央から下方に突出して形成されている。ボス収容部26は後述する揺動スクロール25のボス25Cを収容するためのものであり、メインフレーム21の他方の面(上側の面)の中央を下方に凹陥することにより形成されている。駆動軸15の先端(上端)には、偏心軸部15Aが形成されている。この偏心軸部15Aは、中心が駆動軸15の軸心と偏心して設けられると共に、旋回軸受24を介して、ボス25Cに旋回駆動可能に挿入されている。
上記スクロール圧縮機構11は、固定スクロール23と揺動スクロール25とで構成されている。固定スクロール23は、メインフレーム21の上面に密着して配置される。メインフレーム21は、ケーシング本体5の内面に取り付けられ、固定スクロール23は、メインフレーム21にねじ34で締結されて固定されている。揺動スクロール25は、固定スクロール23に噛合し、固定スクロール23と、メインフレーム21との間の形成される揺動空間12内に配置される。ケーシング3内は、メインフレーム21の下方の高圧空間27と、メインフレーム21の上方の吐出空間29とに区画される。各空間27,29は、メインフレーム21及び固定スクロール23の外周に縦に延びて形成された縦溝71を介して連通している。
ケーシング3の上キャップ7には、冷媒回路の冷媒をスクロール圧縮機構11に導く吸入管31が、またケーシング本体5には、ケーシング3内の冷媒をケーシング3外に吐出させる吐出管33がそれぞれ気密状に貫通固定されている。吸入管31は、吐出空間29を上下方向に延び、その内端部はスクロール圧縮機構11の固定スクロール23を貫通して、圧縮室35に連通し、この吸入管31により圧縮室35内に冷媒が吸入される。
ケーシング3の上キャップ7には、冷媒回路の冷媒をスクロール圧縮機構11に導く吸入管31が、またケーシング本体5には、ケーシング3内の冷媒をケーシング3外に吐出させる吐出管33がそれぞれ気密状に貫通固定されている。吸入管31は、吐出空間29を上下方向に延び、その内端部はスクロール圧縮機構11の固定スクロール23を貫通して、圧縮室35に連通し、この吸入管31により圧縮室35内に冷媒が吸入される。
駆動モータ(DC駆動モータ)13は、直流電源からの入力を受けて駆動するDC(Direct Current)モータであり、環状のステータ37と、このステータ37の内側に回転自在に構成されたロータ39とを備える。駆動モータ13は、一定の入力電圧を受け、パルス波のデューティ比、つまり、パルス波を出す周期と出した時のパルス幅と、を制御するPWM(Pulse Width Modulation)インバータによって回転トルクが制御され駆動する。
ロータ39には、駆動軸15を介してスクロール圧縮機構11の揺動スクロール25が駆動連結されている。ステータ37は、ステータコア37Aと、ステータコイル18とから成る。ステータコア37Aは、薄い鉄板を重ね合わせて形成され、内部には、図示は省略したが、複数の溝を有する。ステータコイル18は、複数相のステータ巻線が巻回されて形成され、ステータコア37Aの内部に形成された溝に嵌入されて、ステータコア37Aの上下に備えられる。ステータコイル18は、インシュレータ19の内部に収容されている。ステータコイル18は、不図示の導線を介して電源供給端子53に接続される。
ロータ39には、駆動軸15を介してスクロール圧縮機構11の揺動スクロール25が駆動連結されている。ステータ37は、ステータコア37Aと、ステータコイル18とから成る。ステータコア37Aは、薄い鉄板を重ね合わせて形成され、内部には、図示は省略したが、複数の溝を有する。ステータコイル18は、複数相のステータ巻線が巻回されて形成され、ステータコア37Aの内部に形成された溝に嵌入されて、ステータコア37Aの上下に備えられる。ステータコイル18は、インシュレータ19の内部に収容されている。ステータコイル18は、不図示の導線を介して電源供給端子53に接続される。
ロータ39は、フェライト磁石、或いは、ネオジウム磁石から形成され着磁によって磁化される。ロータ39を磁化させる方法としては、ロータ39をステータ37に内挿した後、ステータ37のステータコイル18を形成するステータ巻き線に電流を流して着磁する巻線着磁、或いは、ロータ39を外部の着磁装置を用いて着磁させた後にステータ37に内挿する外部着磁がある。駆動軸15の内部には、ロータ39の巻線着磁を行う際に、ロータ39の位置決めに用いる、ホルダ(ピンホルダ)58が圧入されている。
ステータ37は、環状のスペーサリング38によってケーシング3の内壁面に支持される。スペーサリング38はケーシング3の内壁面に焼き嵌めによって固定され、ステータ37はスペーサリング38の内壁面に焼き嵌めによって固定される。スペーサリング38の上端面は、ステータ37の上端面よりも下方に設けられる。
ステータ37は、環状のスペーサリング38によってケーシング3の内壁面に支持される。スペーサリング38はケーシング3の内壁面に焼き嵌めによって固定され、ステータ37はスペーサリング38の内壁面に焼き嵌めによって固定される。スペーサリング38の上端面は、ステータ37の上端面よりも下方に設けられる。
駆動モータ13の下方には、駆動軸15の下端部を回転可能に嵌入支持するベアリングプレート8が備えられる。ベアリングプレート8は、円筒状に形成され駆動軸15が嵌入されるボス部8Aと、このボス部8Aに略等間隔に周設され4方向に延び、ケーシング本体5に固定されるアーム部8Bとを備える。つまり、駆動軸15は、ベアリングプレート8によってケーシング3に支持される。ベアリングプレート8は、各アーム部8Bの間に形成され、上下の空間を連通する開口部8Eを有する。
図1に示す、ベアリングプレート8の下方の下部空間(油溜め)40は、高圧に保たれており、その下端部に相当する下キャップ9の内底部には油が貯留される。ベアリングプレート8と、油溜め40の間には、環状プレート59がベアリングプレート8に固定されて備えられる。また、環状プレート59の上方には、バッフル板14が環状プレート59に支持されて設けられる。バッフル板14は、例えば、多数の細孔14Dを有した、例えば薄板状のパンチングメタルによって形成される。
図1に示す、ベアリングプレート8の下方の下部空間(油溜め)40は、高圧に保たれており、その下端部に相当する下キャップ9の内底部には油が貯留される。ベアリングプレート8と、油溜め40の間には、環状プレート59がベアリングプレート8に固定されて備えられる。また、環状プレート59の上方には、バッフル板14が環状プレート59に支持されて設けられる。バッフル板14は、例えば、多数の細孔14Dを有した、例えば薄板状のパンチングメタルによって形成される。
駆動軸15内には、高圧油供給手段の一部としての給油路41が形成され、この給油路41は、駆動軸15の内部を上下に延び、揺動スクロール25の背面の油室43に連通している。この給油路41は、駆動軸15の下端に設けたオイルピックアップ45に連結される。オイルピックアップ45の奥側には、駆動軸15の径方向に延び、給油路41を貫通する横穴57が設けられる。この横穴57には、上述したホルダ58が圧入される。オイルピックアップ45は、ロータ39の着磁後に、駆動軸15に圧入される。
オイルピックアップ45は、下端に設けられた吸込口42と、この吸込口42の上方に形成されたパドル44とを備える。オイルピックアップ45の下端は、油溜め40に貯留された潤滑オイルに浸漬されて、当該給油路41の吸込口42が潤滑オイル内にて開口している。駆動軸15が回転すると、油溜め40に貯留された潤滑オイルがオイルピックアップ45の吸込口42から給油路41に入り、この給油路41のパドル44に沿って上方に汲み上げられる。そして、汲み上げられた潤滑オイルは、給油路41を通じ、ラジアル軸受部28、及び、旋回軸受24等のスクロール圧縮機構11の各摺動部分に供給される。さらに、潤滑オイルは、給油路41を通じて揺動スクロール25背面の油室43に供給され、この油室43から、揺動スクロール25に設けられた連通路51を介して、圧縮室35へ供給される。
オイルピックアップ45は、下端に設けられた吸込口42と、この吸込口42の上方に形成されたパドル44とを備える。オイルピックアップ45の下端は、油溜め40に貯留された潤滑オイルに浸漬されて、当該給油路41の吸込口42が潤滑オイル内にて開口している。駆動軸15が回転すると、油溜め40に貯留された潤滑オイルがオイルピックアップ45の吸込口42から給油路41に入り、この給油路41のパドル44に沿って上方に汲み上げられる。そして、汲み上げられた潤滑オイルは、給油路41を通じ、ラジアル軸受部28、及び、旋回軸受24等のスクロール圧縮機構11の各摺動部分に供給される。さらに、潤滑オイルは、給油路41を通じて揺動スクロール25背面の油室43に供給され、この油室43から、揺動スクロール25に設けられた連通路51を介して、圧縮室35へ供給される。
メインフレーム21には、ボス収容部26からメインフレーム21を径方向に貫通し、縦溝71に開口する戻し油路47が形成される。給油路41を通じ、スクロール圧縮機構11の各摺動部分、及び、圧縮室35に供給される潤滑オイルのうち、過剰となった潤滑オイルは、この戻し油路47を通って油溜め40に戻される。戻し油路47の下方には、オイルコレクター46が設けられ、オイルコレクター46は、スペーサリング38の上端近傍まで延在する。ステータ37の外周面には、ステータ37の上下に亘る複数の切欠き54が形成される。戻し油路47、オイルコレクター46を通じて給油路41から戻された潤滑オイルは、この切欠き54、及び、ベアリングプレート8の各アーム部8Bの間を通って油溜め40に戻される。なお、図1の断面図において、吐出管33が説明の便宜上破線で示されているが、吐出管33は、オイルコレクター46とは、位相をずらして配置される。
固定スクロール23は、鏡板23Aと、この鏡板23Aの下面に形成された渦巻き状(インボリュート状)のラップ23Bとで構成されている。一方、揺動スクロール25は、鏡板25Aと、この鏡板25Aの上面に形成された渦巻き状(インボリュート状)のラップ25Bとで構成されている。そして、固定スクロール23のラップ23Bと、揺動スクロール25のラップ25Bとは互いに噛合しており、このことにより固定スクロール23と揺動スクロール25との間において、両ラップ23B,25Bで複数の圧縮室35が形成されている。
揺動スクロール25は、オルダムリング61を介して固定スクロール23に支持され、その鏡板25Aの下面の中心部には有底円筒状のボス25Cが突設されている。一方、駆動軸15の上端には偏心軸部15Aが設けられ、この偏心軸部15Aは、揺動スクロール25のボス25Cに回転可能に嵌入されている。
さらに、駆動軸15には、メインフレーム21の下側に、カウンタウェイト部(上バランサ)63が設けられ、ロータ39の下部には、下バランサ77が設けられている。駆動軸15は、これらの上バランサ63、及び、下バランサ77によって揺動スクロール25や偏心軸部15A等と動的バランスを取っている。これらの上バランサ63、及び、下バランサ77により重さのバランスを取りながら駆動軸15が回転することで、揺動スクロール25を公転させるようになっている。そして、この揺動スクロール25の公転に伴い、圧縮室35は、両ラップ23B,25B間の容積が中心に向かって収縮することで吸入管31より吸入された冷媒を圧縮するように構成されている。また、下バランサ77の下面には、ロータ39、及び、下バランサ77と一体にカシメられる規制プレート55が設けられる。規制プレート55はロータ39の巻線着磁を行う際に、ロータ39の回転を規制する。
メインフレーム21の下側には、上バランサ63の周りを囲うようにカップ48がボルト49で固定されている。カップ48は、メインフレーム21と、駆動軸15との間のクリアランスから漏れ出た潤滑オイルが、上バランサ63の回転によって吐出管側に飛散されるのを防ぐ。
固定スクロール23の中央部には吐出孔73が設けられており、この吐出孔73から吐出されたガス冷媒は、吐出弁75を通って吐出空間29に吐出され、メインフレーム21及び固定スクロール23の各外周に設けた縦溝71を介して、メインフレーム21の下方の高圧空間27に流出し、この高圧冷媒は、ケーシング本体5に設けた吐出管33を介してケーシング3外に吐出される。
固定スクロール23の中央部には吐出孔73が設けられており、この吐出孔73から吐出されたガス冷媒は、吐出弁75を通って吐出空間29に吐出され、メインフレーム21及び固定スクロール23の各外周に設けた縦溝71を介して、メインフレーム21の下方の高圧空間27に流出し、この高圧冷媒は、ケーシング本体5に設けた吐出管33を介してケーシング3外に吐出される。
ところで、上述したように、ステータ37は、環状のスペーサリング38によってケーシング3の内壁面に支持される。スペーサリング38はケーシング3の内壁面に焼き嵌めによって固定され、ステータ37はスペーサリング38の内壁面に焼き嵌めによって固定される。スペーサリング38は薄肉のリング体38A(図5、図6参照。)であり、このリング体38Aを製造する場合、予め粗加工されたリング体38Aの外周面および内周面を加工機により仕上げ加工する。
本実施の形態では、仕上げ加工の段階で、加工機のチャックに治具を介してリング体38Aを把持して外周面を加工した後、アンクランプせずに、同一の治具によりリング体38Aを把持して内周面を加工できる。
本実施の形態では、仕上げ加工の段階で、加工機のチャックに治具を介してリング体38Aを把持して外周面を加工した後、アンクランプせずに、同一の治具によりリング体38Aを把持して内周面を加工できる。
図2は、本実施の形態によるリング体把持治具を示し、図3は、リング体38Aの内周面加工時のリング体把持治具を示し、図4は、リング体38Aの外周面加工時のリング体把持治具を示す。
図2~図4に示すように、リング体把持治具80は、中実円盤状の把持治具本体81を備え、この把持治具本体81は、加工機150のチャック151に固定される。チャック151は、周方向に120°の等間隔で配置され、径方向に移動して把持治具本体81の外周面を把持する。
図5は、図3に対応する、リング体38Aの内周面加工時のリング体把持治具を示す。図5A,図5Bに示すように、把持治具本体81は、加工機のチャック151に固定される固定面81Aを有し、反対側の把持面81Bには、周方向に90°の等間隔で4つの雌ねじ穴81Cが形成されている。
雌ねじ穴81Cには把持面81Bから突出してボルト82が締結され、ボルト82の先端にはリング体38Aの端面を外側から押さえる爪部材83と、支持ピン84とが配置されている。支持ピン84は基端が爪部材83の外端にねじ込まれ、先端が把持面81Bに当接自在となっている。雌ねじ穴81C、ボルト82、爪部材83、支持ピン84などが把持機構部を構成する。
この把持機構部は、リング体38Aの内周面加工時に、把持治具本体81の把持面81Bに取り付けられる把持機構部である。
図5Aに示すように、加工機のチャック151に固定した把持治具本体81の把持面81Bに、まず、リング体38Aを宛がい、リング体38Aの端面に爪部材83を配置し、爪部材83の外端に支持ピン84を配置した状態で、ボルト82を螺入して、リング体38Aの端面を押圧し、把持面81Bと爪部材83との間にリング体38Aを狭持する。4つの爪部材83をすべてボルト82によりねじ込むと、リング体38Aは堅固に狭持される。
このとき、爪部材83の内端はリング体38Aの内径にかからないように構成されており、加工機の加工工具を矢印Aの方向に挿入した後、該工具を矢印Bの方向に送って内周面が内径加工される。
図5Aに示すように、加工機のチャック151に固定した把持治具本体81の把持面81Bに、まず、リング体38Aを宛がい、リング体38Aの端面に爪部材83を配置し、爪部材83の外端に支持ピン84を配置した状態で、ボルト82を螺入して、リング体38Aの端面を押圧し、把持面81Bと爪部材83との間にリング体38Aを狭持する。4つの爪部材83をすべてボルト82によりねじ込むと、リング体38Aは堅固に狭持される。
このとき、爪部材83の内端はリング体38Aの内径にかからないように構成されており、加工機の加工工具を矢印Aの方向に挿入した後、該工具を矢印Bの方向に送って内周面が内径加工される。
図6は、図4に対応する、リング体38Aの外周面加工時のリング体把持治具を示す。図6A,図6Bに示すように、把持治具本体81は、加工機のチャック151に固定される固定面81Aを有し、反対側の把持面81Bのセンターに、雌ねじ穴(被締結部)81Dが形成されている。
雌ねじ穴81Dにはボルト85が締結され、ボルト85は、リング体38Aの端面を把持治具本体81の把持面81Bに向けて押圧する押さえ板87を止めるための締結具を構成する。押さえ板87は、リング体38Aの外周面加工時に、リング体38Aを把持治具本体81の把持面81Bに押圧するための部材であり、その外径はリング体38Aの外径よりも小さく、その外周部には、周方向に90°の等間隔で4つの半円弧状の凹所87Aが形成され、この凹所87Aには後述するように上記爪部材83の先端部83Aが嵌合自在となっている。押さえ板87によりリング体38Aが把持されると、加工機の加工工具が、矢印Aの方向に移動し、該工具を矢印Bの方向に送って外周面が外径加工される。
雌ねじ穴81Dにはボルト85が締結され、ボルト85は、リング体38Aの端面を把持治具本体81の把持面81Bに向けて押圧する押さえ板87を止めるための締結具を構成する。押さえ板87は、リング体38Aの外周面加工時に、リング体38Aを把持治具本体81の把持面81Bに押圧するための部材であり、その外径はリング体38Aの外径よりも小さく、その外周部には、周方向に90°の等間隔で4つの半円弧状の凹所87Aが形成され、この凹所87Aには後述するように上記爪部材83の先端部83Aが嵌合自在となっている。押さえ板87によりリング体38Aが把持されると、加工機の加工工具が、矢印Aの方向に移動し、該工具を矢印Bの方向に送って外周面が外径加工される。
本実施の形態では、把持治具本体81にリング体38Aを把持したまま、把持機構部による把持、すなわち図5に示すように、雌ねじ穴81C、ボルト82、爪部材83、支持ピン84などによる把持と、図6に示すように、押さえ板87による把持とを切り替え可能に構成されている。
例えば、スペーサリング38の仕上げ加工の段階で、最初にリング体38Aの内径加工を行い、ついで外径加工を行う場合、まず図5に示すように、雌ねじ穴81C、ボルト82、爪部材83、支持ピン84などによりリング体38Aを把持して、加工工具を矢印Aの方向に挿入した後、該工具を矢印Bの方向に送ってリング体38Aの内周面を内径加工する。
ついでリング体38Aを、図5に示すように把持した状態のまま、図6に示すように、押さえ板87を、凹所87Aが雌ねじ穴81Cに対向するように微調節して、リング体38Aの端面に宛がう。そして、押さえ板87の外周部の凹所87Aに爪部材83の先端部83Aが位置するように爪部材83を配置し、この爪部材83をボルト82により止着して、リング体38Aを把持する。その後に、リング体38Aの外径加工のために、図5の把持機構部を撤去し、すなわち図6に示す把持状態のままとして、加工機の加工工具を、矢印Aの方向に移動し、該工具を矢印Bの方向に送って外周面を外径加工する。
本実施の形態では、把持治具本体81にリング体38Aを把持したまま、図5の把持機構部による把持と、図6に示す押さえ板87による把持とを切り替え可能に構成されているため、従来のように別治具を用いてリング体38Aを把持し直す必要がなく、リング体38Aを把持し直す際に生じる位置ずれがなくなり、リング体38Aの内径および外径の同軸度を確保でき、芯精度のくるいが解消でき、精度の良いリング体38Aを製造することができる。従って、スペーサリング38を用いて、ケーシング内部にステータ37を精度良く支持できる。
以上、一実施の形態に基づいて本発明を説明したが、本発明はこれに限定されるものではない。本実施の形態では、スクロール圧縮機におけるスペーサリング38の製造について説明したが、本発明は、スペーサリング38に限らず、一般の機械要素として、特に薄肉のすべてのリング体製造に好適である。また、上記の説明では、図5の内周面加工から、図6の外周面加工への手順について説明したが、これとは反対に、図6の外周面加工から、図5の内周面加工への手順についても、同様に、内径および外径の同軸度を容易に確保できる。
38 スペーサリング
38A リング体
80 リング体把持治具
81 把持治具本体
81A 固定面
81B 把持面
81C 雌ねじ穴
81D 雌ねじ穴(被締結部)
82 ボルト(把持機構部)
83 爪部材(把持機構部)
83A 先端部
84 支持ピン(把持機構部)
85 ボルト(締結具)
87 押さえ板
87A 凹所
150 加工機
151 チャック
38A リング体
80 リング体把持治具
81 把持治具本体
81A 固定面
81B 把持面
81C 雌ねじ穴
81D 雌ねじ穴(被締結部)
82 ボルト(把持機構部)
83 爪部材(把持機構部)
83A 先端部
84 支持ピン(把持機構部)
85 ボルト(締結具)
87 押さえ板
87A 凹所
150 加工機
151 チャック
Claims (6)
- リング体の外周面および/または内周面を機械加工する際に当該リング体を把持するリング体把持治具において、
加工機のチャックに固定される固定面を有した把持治具本体と、
前記リング体の内周面加工時に前記把持治具本体の把持面から突設され先端に当該リング体の端面を外側から押さえる爪部材を有した把持機構部と、
前記リング体の外周面加工時に当該リング体の端面を前記把持治具本体の把持面に向けて押圧する押さえ板を止める締結具が締結される被締結部とを備えた、
ことを特徴とするリング体把持治具。 - 前記把持機構部が前記爪部材と当該爪部材を前記把持治具本体に連結するボルトとを備え、前記把持治具本体の把持面に前記ボルトに対応した雌ねじ穴が形成されていることを特徴とする請求項1に記載のリング体把持治具。
- 前記押さえ板の外周部に前記爪部材の先端部が嵌合自在な凹所が形成されていることを特徴とする請求項1または2に記載のリング体把持治具。
- 前記把持治具本体に前記リング体を把持したまま、前記把持機構部による把持と、前記押さえ板による把持とを切り替え可能に構成されていることを特徴とする請求項1ないし3のいずれか一項に記載のリング体把持治具。
- 前記把持治具本体に前記リング体を把持したまま、内周面加工から外周面加工へ、あるいは外周面加工から内周面加工へ切り替え可能に構成されていることを特徴とする請求項1ないし3のいずれか一項に記載のリング体把持治具。
- ケーシングの内部に冷媒を圧縮するスクロール圧縮機構と、前記スクロール圧縮機構と駆動軸で連結され当該スクロール圧縮機構を駆動する駆動モータとが収容され、前記スクロール圧縮機構がメインフレームにより前記ケーシングに支持され、前記駆動モータのロータに前記駆動軸が連結され、当該駆動軸がベアリングプレートにより前記ケーシングに支持され、前記モータのステータは請求項1ないし5のいずれか一項に記載のリング体把持治具を利用して加工形成された後、前記ケーシングに支持されたことを特徴とするスクロール圧縮装置。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2011800693476A CN103429900A (zh) | 2011-03-24 | 2011-12-20 | 环形体把持夹具及涡旋压缩装置 |
Applications Claiming Priority (8)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2011-065607 | 2011-03-24 | ||
| JP2011065607A JP2012202252A (ja) | 2011-03-24 | 2011-03-24 | スクロール圧縮装置 |
| JP2011066920A JP2012202277A (ja) | 2011-03-25 | 2011-03-25 | スクロール圧縮装置 |
| JP2011-066920 | 2011-03-25 | ||
| JP2011-066921 | 2011-03-25 | ||
| JP2011-067051 | 2011-03-25 | ||
| JP2011066921A JP2012202278A (ja) | 2011-03-25 | 2011-03-25 | スクロール圧縮装置、及び、スクロール圧縮装置の着磁方法 |
| JP2011067051A JP5824668B2 (ja) | 2011-03-25 | 2011-03-25 | リング体把持治具及びスクロール圧縮装置 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2012127752A1 true WO2012127752A1 (ja) | 2012-09-27 |
Family
ID=46878937
Family Applications (3)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2011/079466 Ceased WO2012127752A1 (ja) | 2011-03-24 | 2011-12-20 | リング体把持治具及びスクロール圧縮装置 |
| PCT/JP2011/079464 Ceased WO2012127750A1 (ja) | 2011-03-24 | 2011-12-20 | スクロール圧縮装置 |
| PCT/JP2011/079465 Ceased WO2012127751A1 (ja) | 2011-03-24 | 2011-12-20 | スクロール圧縮装置、及び、スクロール圧縮装置の着磁方法 |
Family Applications After (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2011/079464 Ceased WO2012127750A1 (ja) | 2011-03-24 | 2011-12-20 | スクロール圧縮装置 |
| PCT/JP2011/079465 Ceased WO2012127751A1 (ja) | 2011-03-24 | 2011-12-20 | スクロール圧縮装置、及び、スクロール圧縮装置の着磁方法 |
Country Status (3)
| Country | Link |
|---|---|
| US (2) | US20140064995A1 (ja) |
| CN (3) | CN103477077B (ja) |
| WO (3) | WO2012127752A1 (ja) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104209775A (zh) * | 2014-08-08 | 2014-12-17 | 安徽昱工耐磨材料科技有限公司 | 外斜面辊皮环装夹装置 |
Families Citing this family (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104343689A (zh) * | 2013-08-06 | 2015-02-11 | 珠海格力节能环保制冷技术研究中心有限公司 | 涡旋压缩机的压缩总成及涡旋压缩机 |
| CN105443393A (zh) * | 2014-05-29 | 2016-03-30 | 丹佛斯(天津)有限公司 | 压缩机的回油装置及压缩机 |
| KR102243681B1 (ko) * | 2014-08-13 | 2021-04-23 | 엘지전자 주식회사 | 스크롤 압축기 |
| JP7035464B2 (ja) * | 2017-01-20 | 2022-03-15 | 株式会社ジェイテクト | 切削加工方法及び切削加工装置 |
| JP6927164B2 (ja) | 2018-06-29 | 2021-08-25 | 株式会社デンソー | 横置きスクロールコンプレッサ |
| CN110005611B (zh) * | 2019-05-30 | 2020-04-10 | 浙江科技学院 | 涡旋机及其电磁机构和控制方法 |
| CN110185616B (zh) * | 2019-05-30 | 2020-04-14 | 浙江科技学院 | 涡旋机及其电磁机构和电磁机构的电磁气隙寻优方法 |
| JP7401754B2 (ja) * | 2020-01-31 | 2023-12-20 | ダイキン工業株式会社 | 油分離部材を備えるスクロール圧縮機 |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS58165907A (ja) * | 1982-03-24 | 1983-10-01 | Toshiba Corp | 旋削加工ワ−クの把握装置 |
| JP2006212746A (ja) * | 2005-02-04 | 2006-08-17 | Murata Mach Ltd | 旋盤のチャック装置およびそのチャック装置を用いた加工方法 |
| JP2009097358A (ja) * | 2007-10-12 | 2009-05-07 | Mayekawa Mfg Co Ltd | 密閉スクロール圧縮機およびその組立方法 |
Family Cites Families (47)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5546081A (en) | 1978-09-29 | 1980-03-31 | Mitsubishi Electric Corp | Scroll compressor |
| JPS57212389A (en) * | 1981-06-22 | 1982-12-27 | Hitachi Ltd | Enclosed scroll compressor |
| JPS58117378A (ja) | 1981-12-28 | 1983-07-12 | Mitsubishi Electric Corp | スクロ−ル圧縮機 |
| JPS5929785A (ja) | 1982-08-13 | 1984-02-17 | Mitsubishi Electric Corp | 冷媒圧縮機 |
| JPS6075795A (ja) | 1983-09-30 | 1985-04-30 | Toshiba Corp | スクロ−ル型圧縮装置 |
| JPH06105079B2 (ja) * | 1984-03-30 | 1994-12-21 | 三菱電機株式会社 | スクロール形流体機械 |
| JPS61167354A (ja) | 1985-01-18 | 1986-07-29 | Matsushita Electric Ind Co Ltd | 小型モ−タ |
| JP2817512B2 (ja) | 1992-05-07 | 1998-10-30 | ダイキン工業株式会社 | スクロール圧縮機 |
| JP3283061B2 (ja) * | 1992-06-19 | 2002-05-20 | 株式会社日立製作所 | 旋回スクロールの加工法 |
| US5873710A (en) * | 1997-01-27 | 1999-02-23 | Copeland Corporation | Motor spacer for hermetic motor-compressor |
| JP4126736B2 (ja) | 1997-10-29 | 2008-07-30 | 株式会社日立製作所 | スクロール圧縮機 |
| JP3218217B2 (ja) * | 1998-03-24 | 2001-10-15 | ダイキン工業株式会社 | 永久磁石型電動機、着磁装置およびその着磁方法 |
| JPH11341752A (ja) * | 1998-05-21 | 1999-12-10 | Toshiba Corp | 永久磁石形回転電機の着磁方法 |
| JP3747999B2 (ja) * | 1998-12-01 | 2006-02-22 | 株式会社日立製作所 | スクロール圧縮機 |
| JP2001041184A (ja) * | 1999-08-03 | 2001-02-13 | Daikin Ind Ltd | スクロール流体機械 |
| JP4032697B2 (ja) * | 2001-10-23 | 2008-01-16 | 三菱電機株式会社 | 圧縮機、圧縮機の加工方法 |
| JP2002199670A (ja) | 2001-11-06 | 2002-07-12 | Sanyo Electric Co Ltd | 直流モータの着磁方法及びコンプレッサ用直流モータの着磁方法 |
| JP3789825B2 (ja) | 2002-01-31 | 2006-06-28 | 三洋電機株式会社 | 電動機用回転子のバランスウエイト及びその重量調整方法及びロータリコンプレッサ |
| JP3984864B2 (ja) | 2002-05-14 | 2007-10-03 | 株式会社日立製作所 | 冷凍装置及び圧縮機 |
| JP2004011473A (ja) * | 2002-06-04 | 2004-01-15 | Sanden Corp | スクロール型電動圧縮機の制御装置 |
| JP3731069B2 (ja) | 2002-07-29 | 2006-01-05 | ダイキン工業株式会社 | 圧縮機 |
| EP1523396B1 (de) * | 2002-08-02 | 2008-02-20 | ABB Turbo Systems AG | Verfahren und vorrichtung zum einspannen rotationssymmetrischer körper |
| CN1281868C (zh) * | 2002-08-27 | 2006-10-25 | Lg电子株式会社 | 涡旋压缩机 |
| JP3896472B2 (ja) | 2002-09-04 | 2007-03-22 | 株式会社日立製作所 | 冷凍装置 |
| JP2004251173A (ja) | 2003-02-19 | 2004-09-09 | Denso Corp | 密閉型電動機付圧縮機 |
| JP2004270544A (ja) | 2003-03-07 | 2004-09-30 | Matsushita Electric Ind Co Ltd | 着磁治具および電動圧縮機ならびに回転子の組み立て方法および電動圧縮機の組み立て方法 |
| JP2004293492A (ja) | 2003-03-28 | 2004-10-21 | Mitsubishi Electric Corp | スクロール流体機械およびその組立方法 |
| JP2004308445A (ja) * | 2003-04-02 | 2004-11-04 | Denso Corp | 電動圧縮機 |
| JP2004332688A (ja) | 2003-05-12 | 2004-11-25 | Matsushita Electric Ind Co Ltd | 電動圧縮機 |
| KR20050067005A (ko) | 2003-12-26 | 2005-06-30 | 마츠시타 덴끼 산교 가부시키가이샤 | 영구자석형 전동기의 착자 방법 및 장치 |
| JP4433184B2 (ja) | 2004-11-05 | 2010-03-17 | 株式会社富士通ゼネラル | 圧縮機 |
| JP2005188519A (ja) | 2005-02-28 | 2005-07-14 | Sanyo Electric Co Ltd | スクロール圧縮機の製造方法 |
| JP4832040B2 (ja) * | 2005-09-20 | 2011-12-07 | 三洋電機株式会社 | 圧縮機 |
| JP2007187049A (ja) | 2006-01-12 | 2007-07-26 | Fujitsu General Ltd | スクロール圧縮機の調芯方法 |
| JP2007228684A (ja) | 2006-02-22 | 2007-09-06 | Daikin Ind Ltd | アウターロータ型モータおよびアウターロータ型モータの着磁方法 |
| KR20080023456A (ko) | 2006-09-11 | 2008-03-14 | 삼성광주전자 주식회사 | 압축기 모터의 마그네트 착자방법 |
| US7413423B2 (en) * | 2006-09-14 | 2008-08-19 | Emerson Climate Technologies, Inc. | Compressor having a lubrication shield |
| JP4799437B2 (ja) | 2007-02-06 | 2011-10-26 | サンデン株式会社 | 流体機械 |
| JP5114710B2 (ja) | 2007-10-16 | 2013-01-09 | 株式会社前川製作所 | 密閉形スクロール圧縮機およびその組立方法 |
| JP2009162078A (ja) * | 2007-12-28 | 2009-07-23 | Daikin Ind Ltd | スクロール型圧縮機 |
| US8235690B2 (en) * | 2008-03-19 | 2012-08-07 | Sanyo Electric Co., Ltd. | Scroll compressor with improved oil separation from refrigerant gas |
| JP5070106B2 (ja) | 2008-03-31 | 2012-11-07 | 三洋電機株式会社 | 圧縮機 |
| JP5066009B2 (ja) | 2008-06-09 | 2012-11-07 | 日立アプライアンス株式会社 | 電動圧縮機 |
| JP5216627B2 (ja) * | 2009-02-20 | 2013-06-19 | 三洋電機株式会社 | スクロール型圧縮機 |
| JP5261227B2 (ja) * | 2009-02-20 | 2013-08-14 | 三洋電機株式会社 | スクロール型圧縮機 |
| JP4687810B2 (ja) | 2009-03-31 | 2011-05-25 | 株式会社富士通ゼネラル | 電動機ロータ |
| JP2011047343A (ja) | 2009-08-28 | 2011-03-10 | Panasonic Corp | 密閉型圧縮機 |
-
2011
- 2011-12-20 WO PCT/JP2011/079466 patent/WO2012127752A1/ja not_active Ceased
- 2011-12-20 WO PCT/JP2011/079464 patent/WO2012127750A1/ja not_active Ceased
- 2011-12-20 CN CN201180069545.2A patent/CN103477077B/zh not_active Expired - Fee Related
- 2011-12-20 WO PCT/JP2011/079465 patent/WO2012127751A1/ja not_active Ceased
- 2011-12-20 CN CN201180069440.7A patent/CN103443463B/zh not_active Expired - Fee Related
- 2011-12-20 CN CN2011800693476A patent/CN103429900A/zh active Pending
- 2011-12-20 US US14/007,171 patent/US20140064995A1/en not_active Abandoned
- 2011-12-20 US US14/007,157 patent/US9581160B2/en not_active Expired - Fee Related
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS58165907A (ja) * | 1982-03-24 | 1983-10-01 | Toshiba Corp | 旋削加工ワ−クの把握装置 |
| JP2006212746A (ja) * | 2005-02-04 | 2006-08-17 | Murata Mach Ltd | 旋盤のチャック装置およびそのチャック装置を用いた加工方法 |
| JP2009097358A (ja) * | 2007-10-12 | 2009-05-07 | Mayekawa Mfg Co Ltd | 密閉スクロール圧縮機およびその組立方法 |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104209775A (zh) * | 2014-08-08 | 2014-12-17 | 安徽昱工耐磨材料科技有限公司 | 外斜面辊皮环装夹装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| CN103443463B (zh) | 2015-12-16 |
| CN103429900A (zh) | 2013-12-04 |
| US20140044572A1 (en) | 2014-02-13 |
| WO2012127751A1 (ja) | 2012-09-27 |
| US9581160B2 (en) | 2017-02-28 |
| WO2012127750A1 (ja) | 2012-09-27 |
| CN103443463A (zh) | 2013-12-11 |
| CN103477077B (zh) | 2015-10-14 |
| US20140064995A1 (en) | 2014-03-06 |
| CN103477077A (zh) | 2013-12-25 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103429900A (zh) | 环形体把持夹具及涡旋压缩装置 | |
| JP5824668B2 (ja) | リング体把持治具及びスクロール圧縮装置 | |
| WO2012127749A1 (ja) | スクロール圧縮装置 | |
| JP2013050079A (ja) | スクロール圧縮装置 | |
| EP3467344A1 (en) | Speed reducer-attached motor | |
| JP5914805B2 (ja) | スクロール圧縮装置 | |
| CN103429898B (zh) | 涡旋压缩装置及涡旋压缩装置的组装方法 | |
| JP2012161878A (ja) | クランクシャフトの加工方法およびロータリ圧縮機の圧縮要素の組立方法 | |
| WO2012127754A1 (ja) | スクロール圧縮装置 | |
| WO2020183896A1 (ja) | 電動圧縮機 | |
| JP2012202278A (ja) | スクロール圧縮装置、及び、スクロール圧縮装置の着磁方法 | |
| JP2020054075A (ja) | 電動機、圧縮機、および冷凍サイクル装置 | |
| JP5818554B2 (ja) | 電動圧縮機 | |
| JP2012207535A (ja) | スクロール圧縮装置 | |
| JP2009243363A (ja) | 圧縮機 | |
| JP2010163882A (ja) | スクロール型流体機械 | |
| JP2012202349A (ja) | スクロール圧縮装置、及び、スクロール圧縮装置における組み立て方法 | |
| JP2004176549A (ja) | 密閉型圧縮機の製造方法 | |
| JP2012202277A (ja) | スクロール圧縮装置 | |
| JP2004239189A (ja) | 密閉型圧縮機の組立方法 | |
| JP2024130012A (ja) | 電動圧縮機 | |
| JP2012207541A (ja) | スクロール圧縮装置 | |
| JP2022148607A (ja) | 圧縮機 | |
| JP2007162497A (ja) | 電動機及び電動機を用いた流体ポンプ | |
| JP2012207603A (ja) | スクロール圧縮装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 11861494 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 11861494 Country of ref document: EP Kind code of ref document: A1 |