WO2020158604A1 - 積層体及びその製造方法、複合積層体の製造方法、並びにポリマーフィルムの製造方法 - Google Patents
積層体及びその製造方法、複合積層体の製造方法、並びにポリマーフィルムの製造方法 Download PDFInfo
- Publication number
- WO2020158604A1 WO2020158604A1 PCT/JP2020/002517 JP2020002517W WO2020158604A1 WO 2020158604 A1 WO2020158604 A1 WO 2020158604A1 JP 2020002517 W JP2020002517 W JP 2020002517W WO 2020158604 A1 WO2020158604 A1 WO 2020158604A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- layer
- metal foil
- polymer
- laminate
- foil layer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/04—Layered products comprising a layer of metal comprising metal as the main or only constituent of a layer, which is next to another layer of the same or of a different material
- B32B15/08—Layered products comprising a layer of metal comprising metal as the main or only constituent of a layer, which is next to another layer of the same or of a different material of synthetic resin
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/02—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29D—PRODUCING PARTICULAR ARTICLES FROM PLASTICS OR FROM SUBSTANCES IN A PLASTIC STATE
- B29D7/00—Producing flat articles, e.g. films or sheets
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/04—Layered products comprising a layer of metal comprising metal as the main or only constituent of a layer, which is next to another layer of the same or of a different material
- B32B15/08—Layered products comprising a layer of metal comprising metal as the main or only constituent of a layer, which is next to another layer of the same or of a different material of synthetic resin
- B32B15/082—Layered products comprising a layer of metal comprising metal as the main or only constituent of a layer, which is next to another layer of the same or of a different material of synthetic resin comprising vinyl resins; comprising acrylic resins
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B27/00—Layered products comprising a layer of synthetic resin
- B32B27/18—Layered products comprising a layer of synthetic resin characterised by the use of special additives
- B32B27/20—Layered products comprising a layer of synthetic resin characterised by the use of special additives using fillers, pigments, thixotroping agents
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B27/00—Layered products comprising a layer of synthetic resin
- B32B27/30—Layered products comprising a layer of synthetic resin comprising vinyl (co)polymers; comprising acrylic (co)polymers
- B32B27/304—Layered products comprising a layer of synthetic resin comprising vinyl (co)polymers; comprising acrylic (co)polymers comprising vinyl halide (co)polymers, e.g. PVC, PVDC, PVF, PVDF
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B3/00—Layered products comprising a layer with external or internal discontinuities or unevennesses, or a layer of non-planar shape; Layered products comprising a layer having particular features of form
- B32B3/26—Layered products comprising a layer with external or internal discontinuities or unevennesses, or a layer of non-planar shape; Layered products comprising a layer having particular features of form characterised by a particular shape of the outline of the cross-section of a continuous layer; characterised by a layer with cavities or internal voids ; characterised by an apertured layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B5/00—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts
- B32B5/02—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts characterised by structural features of a fibrous or filamentary layer
- B32B5/10—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts characterised by structural features of a fibrous or filamentary layer characterised by a fibrous or filamentary layer reinforced with filaments
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B5/00—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts
- B32B5/16—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts characterised by features of a layer formed of particles, e.g. chips, powder or granules
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C26/00—Coating not provided for in groups C23C2/00 - C23C24/00
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D5/00—Electroplating characterised by the process; Pretreatment or after-treatment of workpieces
- C25D5/16—Electroplating with layers of varying thickness
-
- H—ELECTRICITY
- H05—ELECTRIC TECHNIQUES NOT OTHERWISE PROVIDED FOR
- H05K—PRINTED CIRCUITS; CASINGS OR CONSTRUCTIONAL DETAILS OF ELECTRIC APPARATUS; MANUFACTURE OF ASSEMBLAGES OF ELECTRICAL COMPONENTS
- H05K1/00—Printed circuits
- H05K1/02—Details
- H05K1/03—Use of materials for the substrate
-
- H—ELECTRICITY
- H05—ELECTRIC TECHNIQUES NOT OTHERWISE PROVIDED FOR
- H05K—PRINTED CIRCUITS; CASINGS OR CONSTRUCTIONAL DETAILS OF ELECTRIC APPARATUS; MANUFACTURE OF ASSEMBLAGES OF ELECTRICAL COMPONENTS
- H05K1/00—Printed circuits
- H05K1/02—Details
- H05K1/03—Use of materials for the substrate
- H05K1/0313—Organic insulating material
- H05K1/0353—Organic insulating material consisting of two or more materials, e.g. two or more polymers, polymer + filler, + reinforcement
- H05K1/0366—Organic insulating material consisting of two or more materials, e.g. two or more polymers, polymer + filler, + reinforcement reinforced, e.g. by fibres, fabrics
-
- H—ELECTRICITY
- H05—ELECTRIC TECHNIQUES NOT OTHERWISE PROVIDED FOR
- H05K—PRINTED CIRCUITS; CASINGS OR CONSTRUCTIONAL DETAILS OF ELECTRIC APPARATUS; MANUFACTURE OF ASSEMBLAGES OF ELECTRICAL COMPONENTS
- H05K3/00—Apparatus or processes for manufacturing printed circuits
- H05K3/22—Secondary treatment of printed circuits
- H05K3/28—Applying non-metallic protective coatings
- H05K3/285—Permanent coating compositions
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2305/00—Condition, form or state of the layers or laminate
- B32B2305/07—Parts immersed or impregnated in a matrix
- B32B2305/076—Prepregs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2457/00—Electrical equipment
- B32B2457/08—PCBs, i.e. printed circuit boards
Definitions
- the present invention relates to a laminate having a predetermined polymer layer, which is provided in direct contact with the surface of a predetermined metal foil layer, a method for producing the same, a method for producing a composite laminate, and a method for producing a polymer film.
- the surface roughness of copper foil is reduced and a polymer layer using a low dielectric constant polymer is formed for the purpose of lowering the dielectric constant.
- low dielectric constant polymers are generally less polar and have poorer adhesion to other materials.
- the copper foil having a reduced surface roughness has an excessively high surface smoothness, so that the anchor effect of the polymer layer is unlikely to occur and the adhesiveness is poor. Therefore, it is difficult to firmly bond the polymer layer containing the low dielectric constant polymer and the low-roughness copper foil.
- the surface of the copper foil is treated with a surface treatment agent containing a silicon atom such as a silane coupling agent. It is no exaggeration to say that the surface of copper foil used in commercial printed wiring boards is treated with a silane coupling agent.
- a silane coupling agent etrafluoroethylene-based polymers (TFE-based polymers) have been attracting attention as low-dielectric-constant polymers, but TFE-based polymers are particularly poor in adhesiveness with other materials. Therefore, the surface of the copper foil is also treated with a silane coupling agent to enhance the adhesiveness with the copper foil (see Patent Document 1).
- Nickel is excellent as a barrier layer, but its resistivity is higher than that of copper. Therefore, a printed wiring board containing a large amount of nickel has a large transmission loss. Further, since nickel itself is easily denatured at a high temperature, the adhesiveness between the polymer layer and the copper foil is apt to be deteriorated after the high temperature exposure in the manufacturing process of the printed wiring board. In order to solve such a problem, it has been proposed to provide an antioxidant treatment layer containing cobalt and molybdenum on the surface of the copper foil (see Patent Document 4).
- a prepreg is adhered to the TFE polymer layer so as to cover the entire circuit pattern and laminated.
- the adhesive force between the TFE polymer layer and the prepreg is low, and delamination between them tends to occur. Therefore, before adhering the prepreg, the surface of the TFE polymer layer is surface-treated (silane coupling agent treatment, plasma treatment, etc.) to improve the adhesiveness (see Patent Documents 5 and 6).
- the TFE-based polymer is poor in the interaction with the silane coupling agent, the effect of improving the adhesiveness between the TFE-based polymer and the copper foil by the silane coupling agent is not sufficient. It was limited. Further, the silane coupling agent tends to cause variations in its reactivity and variations in the amount attached to the surface of the copper foil, which is an unstable factor in the adhesiveness of the TFE polymer to the copper foil.
- the present inventors have found that the use of a predetermined TFE-based polymer and metal foil makes it possible to eliminate unstable elements by using a silane coupling agent.
- the present inventors when the TFE polymer is used as the low dielectric constant polymer, the initial adhesive strength between the layer containing cobalt and molybdenum and the TFE polymer is extremely low, and the TFE polymer is not easily exposed after exposure to high temperature. The adhesive strength was still not enough. Therefore, as a result of diligent studies to improve the initial adhesive strength, the present inventors have used a metal foil having a surface on which nickel is present in a predetermined trace amount, and a predetermined TFE-based polymer on the surface of the metal foil. It has been found that when a polymer layer containing the same is provided, a laminate having excellent initial adhesive strength and adhesive strength after high temperature exposure and excellent electrical characteristics can be obtained.
- a polymer layer containing a TFE-based polymer that exhibits high adhesiveness to a prepreg can be obtained by using a metal foil having a predetermined surface texture, and completed the present invention. did.
- the present invention provides a laminate in which uniform and high adhesion is obtained between a polymer layer and a metal foil layer, and a method for producing the same.
- the present invention also provides a laminate having excellent electrical properties, which has a high initial adhesive force between the polymer layer and the metal foil layer and maintains a high adhesive force even after a high temperature heat history, and a method for producing the same.
- the present invention provides a method for producing a polymer film that exhibits high adhesion to a prepreg or the like even if surface treatment is omitted, and a method for producing a composite laminate in which peeling between the polymer layer and the prepreg layer is unlikely to occur. For the purpose of providing.
- the present invention has the following aspects.
- a metal foil layer in which no silicon atoms are present on the surface, or a nickel atom ratio detected when fluorescent X-ray analysis is performed on the surface is 0.03 to
- a laminate which is a metal foil layer containing 0.25% by mass.
- the metal foil layer includes a base material layer and a roughening treatment layer having metal particles and having the surface.
- the metal foil layer includes a base material layer and a roughening treatment layer having metal particles and having the surface, and the metal particles are copper, nickel, phosphorus, tungsten, arsenic, molybdenum, or chromium.
- the metal foil layer includes a base material layer and a roughening treatment layer having metal particles and having the surface, and the metal particles include needle-shaped metal particles.
- ⁇ 5> The laminate according to any one of ⁇ 1> to ⁇ 4>, wherein the ten-point average roughness of the surface of the metal foil layer is 0.1 ⁇ m or more.
- the tetrafluoroethylene-based polymer is a tetrafluoroethylene-based polymer containing a unit based on a unit based on perfluoro(alkyl vinyl ether), or polytetrafluoroethylene having a number average molecular weight of 200,000 or less.
- the tetrafluoroethylene-based polymer contains a unit based on perfluoro(alkyl vinyl ether), and a tetrafluoroethylene-based polymer having an oxygen-containing polar group, or a unit based on perfluoro(alkyl vinyl ether) based on all units.
- ⁇ 8> The laminate according to any one of ⁇ 1> to ⁇ 7>, wherein the polymer layer has a peel strength of 10 N/cm or more with respect to the metal foil layer.
- a method for producing a laminated body comprising: forming a polymer layer containing the above in a direct contact, and obtaining a laminated body having the polymer layer provided in direct contact with a surface of a metal foil layer composed of the metal foil.
- the melt viscosity at 380° C. is 1 ⁇ 10 2 to 1 ⁇ 10 6 on the surface of a metal foil in which the proportion of nickel atoms detected by fluorescent X-ray analysis is 0.03 to 0.25 mass %.
- a polymer layer containing a tetrafluoroethylene-based polymer of Pa ⁇ s is formed in direct contact, and a laminate having the polymer layer provided in direct contact with the surface of the metal foil layer composed of the metal foil is obtained. And a method for manufacturing a laminate.
- a method for producing a composite laminate comprising: obtaining a composite laminate in which a solder mask layer and a solder mask layer are laminated. ⁇ 14> The method according to ⁇ 13>, wherein the exposed surface of the polymer layer is treated with an acid solution, and a solder resist is directly applied as it is and cured to form a solder mask layer.
- the laminated body which can obtain uniform and high adhesiveness between a polymer layer and a metal foil, and its manufacturing method are provided. Further, according to the present invention, between the polymer layer and the metal foil, there is a high initial adhesive force, and the high adhesive force is maintained even after a high temperature heat history, and a laminate excellent in electrical characteristics, and the production thereof. A method is provided. Further, according to the present invention, there is provided a polymer film exhibiting a high adhesive force to a prepreg and the like, and a composite laminate in which peeling between the polymer layer and the prepreg layer does not easily occur.
- D50 of powder is a particle size distribution of powder measured by a laser diffraction/scattering method, and a cumulative curve is calculated by setting the total volume of particles constituting the powder (hereinafter, also referred to as "powder particles") as 100%. , The particle diameter at the point where the cumulative volume becomes 50% on the cumulative curve (volume-based cumulative 50% diameter).
- Powder D90 is a point where the particle size distribution of powder is measured by a laser diffraction/scattering method, a cumulative curve is calculated with the total volume of the powder particle group as 100%, and the cumulative volume becomes 90% on the cumulative curve. Is the particle size (volume-based cumulative 90% size).
- D50 and D90 of the powder are the volume-based cumulative 50% diameter and the volume-based cumulative 90% diameter of the powder particles, respectively.
- the “melt viscosity of the polymer” is based on ASTM D 1238, and a sample of the polymer (2 g) which had been heated at the measurement temperature for 5 minutes in advance was loaded with 0.7 MPa using a flow tester and a 2 ⁇ -8L die. It is the value measured by holding at the measurement temperature at.
- the "melting temperature (melting point) of the polymer” is a temperature corresponding to the maximum value of the melting peak of the polymer measured by the differential scanning calorimetry (DSC) method.
- “Viscosity” is a value measured with a B-type viscometer at room temperature (25° C.) under a rotation speed of 30 rpm. The measurement is repeated three times, and the average value of the three measured values is used.
- “Ten-point average roughness (Rzjis)” is a value defined in Annex JA of JIS B 0601:2013.
- “Peeling strength” means fixing a position 50 mm from one end in the length direction of a laminate cut out in a rectangular shape (length 100 mm, width 10 mm), pulling speed 50 mm/min, laminate from one end in the length direction. Is the maximum load (N/cm) applied when the metal foil and the polymer layer are separated from each other at 90°.
- the “unit” in a polymer may be an atomic group formed directly from a monomer by a polymerization reaction, and the polymer obtained by the polymerization reaction is treated by a predetermined method to convert an atomic group in which a part of the structure is converted. May be The unit based on the monomer A contained in the polymer is also simply referred to as “monomer A unit”.
- the laminate of the present invention (this laminate) is provided in direct contact with the metal foil layer and the surface of the metal foil layer, and has a melt viscosity at 380° C. of 1 ⁇ 10 2 to 1 ⁇ 10 6 Pa ⁇ s.
- a polymer layer (hereinafter, also referred to as “F layer”) containing a fluoroethylene polymer (hereinafter, also referred to as “F polymer”).
- the metal foil layer in the present laminate is a metal foil layer having no silicon atom on the surface (hereinafter, also referred to as “metal foil layer 1”), or a nickel atom detected when the surface is subjected to fluorescent X-ray analysis.
- metal foil layer 2 Is 0.03 to 0.25% by mass (hereinafter, also referred to as "metal foil layer 2").
- the present laminate having the metal foil layer 1 will be referred to as the present laminate 1
- the present laminate having the metal foil layer 2 will be referred to as the present laminate 2.
- the laminate 1 has a metal foil layer 1 and an F layer provided in direct contact with the surface of the metal foil layer 1.
- the F layer may be provided on only one surface of the metal foil layer 1 or on both surfaces.
- no silicon atom is present on the surface of the metal foil layer 1 (surface on the F layer side).
- the manufacturing method of the present laminate 1 is a method of forming the F layer by directly contacting the surface of the metal foil layer 1 without treating the surface with the silane coupling agent.
- XRF fluorescent X-ray analysis
- the metal foil constituting the metal foil layer 1 has an oxide (hydroxide or the like) generated by oxidation on its surface.
- an F polymer having a predetermined melt viscosity is likely to interact with an oxide and/or a metal atom present on the surface of the metal foil, and particularly when the F polymer contains an oxygen-containing polar group, the oxygen-containing polar group Is believed to interact strongly with oxides and/or metal atoms present on the surface of the metal foil.
- the F layer containing the F polymer exhibited high adhesiveness with the metal foil.
- the treatment with the silane coupling agent is performed by utilizing the wetting and spreading of the solution containing the silane coupling agent on the surface of the metal foil. Therefore, in the initial stage, the solution is likely to collect in the portion where the silane coupling agent is bound, and the portion where the silane coupling agent is bound and the portion where the silane coupling agent is not bound are scattered like islands, and are present on the surface of the metal foil. It is considered that the amount of the silane coupling agent varies. Moreover, the degree is greatly influenced by the surface properties of the metal foil. Therefore, when the F layer is formed on the surface of the metal foil in such a state, uniform adhesiveness between the F layer and the metal foil is unlikely to be exhibited.
- the present laminate 1 since the surface of the metal foil is not treated with the silane coupling agent, it is possible to prevent the above inconvenience from occurring, and to prevent the occurrence of the above-mentioned inconvenience between the F layer and the metal foil (metal foil layer 1). It is presumed that uniform adhesiveness was obtained.
- This laminate 2 has a metal foil layer 2 and an F layer provided in direct contact with the surface of the metal foil layer 2.
- the F layer may be provided on only one surface of the metal foil layer 2 or on both surfaces.
- a predetermined amount (trace amount) of nickel atoms is present on the surface of the metal foil layer 2 (surface on the F layer side).
- the manufacturing method of the present laminate 2 is a method of forming the F layer by directly contacting the surface of the metal foil on which nickel atoms are present in a predetermined amount.
- the proportion of nickel atoms present on the surface of the metal foil can be measured by analyzing the surface of the metal foil by a fluorescent X-ray analysis (XRF) method.
- XRF fluorescent X-ray analysis
- the metal foil forming the metal foil layer 2 has nickel oxide (hydroxide or the like) formed on the surface thereof by oxidation.
- nickel oxide hydrogen oxide or the like
- an F polymer having a predetermined melt viscosity is likely to interact strongly with the oxide or nickel atom present on the surface of the metal foil, and particularly when the F polymer contains an oxygen-containing polar group, the oxygen-containing polar group It is considered that the group strongly interacts with this oxide or nickel atom.
- the F layer containing the F polymer exhibited high initial adhesiveness with the metal foil (metal foil layer 2).
- the presence of nickel atoms exerts an effect of preventing deterioration (corrosion) of the surface of the metal foil due to the F polymer. For this reason, it is presumed that the present laminate 2 maintained a high adhesive force between the F layer and the metal foil (metal foil layer 2) even after the thermal history at high temperature.
- the F polymer in the present invention is a polymer containing a unit based on tetrafluoroethylene (TFE) (TFE unit), and is preferably a hot melt processable polymer.
- the melt viscosity of the F polymer at 380° C. is 1 ⁇ 10 2 to 1 ⁇ 10 6 Pa ⁇ s, preferably 1 ⁇ 10 3 to 1 ⁇ 10 6 Pa ⁇ s.
- the melting temperature of the F polymer is preferably 140 to 320°C, more preferably 200 to 320°C, and further preferably 260 to 320°C. In this case, it is easy to further improve the adhesiveness of the F layer to the metal foil (metal foil layers 1 and 2).
- the F polymer preferably has an oxygen-containing polar group.
- the oxygen-containing polar group possessed by the F polymer may be contained in a unit based on the monomer having the oxygen-containing polar group, may be contained in the terminal portion of the polymer main chain, and may be subjected to surface treatment (radiation treatment, electron beam treatment). , Corona treatment, plasma treatment, etc.), and the former is preferable.
- the oxygen-containing polar group contained in the F polymer may be a group prepared by modifying a polymer having a group capable of forming an oxygen-containing polar group.
- the oxygen-containing polar group contained in the polymer terminal group can be obtained by adjusting the components (polymerization initiator, chain transfer agent, etc.) used in the polymerization of the polymer.
- the oxygen-containing polar group is a polar atomic group containing an oxygen atom.
- the oxygen-containing polar group in the present invention does not include the ester bond itself and the ether bond itself, but includes an atomic group containing these bonds as a characteristic group.
- the oxygen-containing polar group is preferably at least one group selected from the group consisting of a hydroxyl group-containing group, a carbonyl group-containing group, an acetal group and an oxycycloalkane group, more preferably a hydroxyl group-containing group or a carbonyl group-containing group, and -CF 2 CH 2 OH, —C(CF 3 ) 2 OH, 1,2-glycol group (—CH(OH)CH 2 OH), —CF 2 C(O)OH, >CFC(O)OH, carboxamide group (-C(O)NH 2, etc.), acid anhydride residue (-C(O)OC(O)-), imide residue (-C(O)NHC(O)-, etc.), dicarboxylic acid residue (—CH(C(O)OH)CH 2 C(O)OH) or a carbonate group (—OC(O)O—) is more preferable.
- the oxygen-containing polar group is a polar group and is a cyclic group or a ring-opening group thereof, a cyclic acid anhydride residue, a cyclic imide residue, A cyclic carbonate group, a cyclic acetal group, a 1,2-dicarboxylic acid residue or a 1,2-glycol group is particularly preferred, and a cyclic acid anhydride residue is most preferred.
- the oxycycloalkane group is preferably an epoxy group or an oxetanyl group.
- the F polymer includes a TFE unit, a unit based on hexafluoropropylene (HFP), perfluoro(alkyl vinyl ether) (PAVE) or fluoroalkyl ethylene (FAE) (hereinafter, also referred to as “PAE unit”), and an oxygen-containing polar group.
- a polymer containing a unit based on a monomer having (hereinafter, also referred to as “polar unit”) is preferable.
- the proportion of TFE units is preferably 50 to 99 mol%, and particularly preferably 90 to 99 mol%, based on all units constituting the F polymer.
- the PAE units are preferably units based on PAVE or units based on HFP, particularly preferably units based on PAVE. Two or more types of PAE units may be used.
- the proportion of PAE units is preferably 0.5 to 9.97 mol%, and more preferably 0.5 to 9.97 mol%, based on all units constituting the F polymer.
- the polar unit is preferably a unit based on a monomer having an acid anhydride residue, a carbonate group, a cyclic acetal group, a 1,2-dicarboxylic acid residue, a 1,2-diol residue, or a 1,3-diol residue.
- a monomer unit having a cyclic acid anhydride residue or a cyclic carbonate group is more preferable, and a monomer unit having a cyclic acid anhydride residue is more preferable.
- the polarity unit may be one type or two or more types.
- Examples of the monomer having a cyclic acid anhydride residue include itaconic anhydride, citraconic anhydride, 5-norbornene-2,3-dicarboxylic acid anhydride (also called hymic acid anhydride; hereinafter also referred to as “NAH”) or maleic anhydride. Acids are preferred and NAH is more preferred.
- the proportion of polar units is preferably 0.01 to 3 mol% based on all units constituting the F polymer.
- the F polymer in this case may further include units other than TFE units, PAE units, and polar units (hereinafter, also referred to as “other units”).
- the other unit may be one type or two or more types.
- Examples of the monomer that forms another unit include ethylene, propylene, vinyl chloride, vinylidene chloride, vinyl fluoride, vinylidene fluoride (VDF), and chlorotrifluoroethylene (CTFE).
- Other units are preferably ethylene, VDF or CTFE, more preferably ethylene.
- the proportion of the other units in the F polymer is preferably 0 to 50 mol %, more preferably 0 to 40 mol% based on all the units constituting the F polymer.
- Preferable embodiments of the F polymer include F polymers containing units based on PAVE (PAVE units), or PTFE having a number average molecular weight of 200,000 or less.
- the number average molecular weight of PTFE is a value calculated based on the following formula (1).
- Mn 2.1 ⁇ 10 10 ⁇ Hc ⁇ 5.16 ...
- Mn represents the number average molecular weight of the above PTFE
- ⁇ Hc represents the heat of crystallization (cal/g) of the above PTFE measured by the differential scanning calorimetry.
- the Mn of PTFE is preferably 10 or less, more preferably 50,000 or less.
- the Mn of PTFE is preferably 10,000 or more.
- a more preferable embodiment of the F polymer is a F polymer containing units based on PAVE and having an oxygen-containing polar group, or an F polymer containing 2.0 to 5.0 mol% of units based on PAVE, and oxygen.
- An F polymer having no contained polar group may be mentioned.
- the F polymer of this embodiment is likely to form fine spherulites in the F layer and is likely to have high adhesion with other components.
- the former polymer preferably contains 90 to 99 mol% of TFE units, 0.5 to 9.97 mol% of PAVE units and 0.01 to 3 mol% of polar units based on all units. ..
- the content of PAVE units in the latter polymer is preferably 2.1 mol% or more, and more preferably 2.2 mol% or more, based on all units.
- the latter polymer is composed of only TFE units and PAVE units, and preferably contains 95.0 to 98.0 mol% of TFE units and 2.0 to 5.0 mol% of PAVE units based on the total units. ..
- the latter polymer does not have an oxygen-containing polar group means that the polymer has less than 500 oxygen-containing polar groups per 1 ⁇ 10 6 carbon atoms constituting the polymer main chain. Means there is.
- the number of oxygen-containing polar groups is preferably 100 or less, more preferably 50 or less.
- the lower limit of the number of oxygen-containing polar groups is usually 0.
- the latter polymer may be produced by using a polymerization initiator, a chain transfer agent, or the like that does not generate an oxygen-containing polar group as a terminal group of the polymer chain. It may be produced by fluorinating an F polymer or the like having an oxygen-containing polar group derived from it as an end group of the polymer main chain. Examples of the fluorination treatment method include a method using fluorine gas (see JP-A-2019-194314, etc.).
- the metal constituting the metal foils to be the metal foil layers 1 and 2 copper, iron, nickel, aluminum, zinc, alloys thereof (copper alloy, stainless steel, nickel alloy (including 42 alloy), aluminum alloy). Etc.) can be mentioned.
- a copper foil is preferable, a rolled copper foil having no distinction between front and back and a copper foil such as an electrolytic copper foil having distinction between front and back are more preferable, and a rolled copper foil is further preferable. Since the rolled copper foil has a small surface roughness, the transmission loss can be reduced even when the laminated body is processed into a printed wiring board.
- the rolled copper foil is preferably used after being immersed in a hydrocarbon-based organic solvent to remove the rolling oil.
- the surface on which the F layer is formed may be any surface in the rolled copper foil, and may be either the deposition surface or the glossy surface in the electrolytic copper foil.
- the metal foil may be a metal foil with a carrier that is laminated on the carrier via an intermediate layer.
- the metal foil may have a laminated structure including a base material layer (for example, copper foil) made of the above metal, and a roughening treatment layer made of metal particles (roughening particles).
- the surface of the roughening treatment layer constitutes the surface of the metal foil.
- the roughening treatment layer include a roughening treatment layer composed of nickel-containing metal particles (roughening particles).
- the metal particles are preferably formed of copper, nickel, phosphorus, tungsten, arsenic, molybdenum, chromium, cobalt, zinc or an alloy containing one or more of these, and copper, nickel, cobalt or one or more of these is used. More preferably, it is formed of an alloy containing.
- the metal particles are more preferably formed of nickel alone or an alloy of nickel and at least one of copper, phosphorus, tungsten, arsenic, molybdenum, chromium, cobalt and zinc, and at least nickel, at least copper and cobalt. Most preferably, it is formed of an alloy containing one type. Such metal particles have excellent adhesion to the metal (especially copper) that constitutes the base material layer.
- the roughening treatment layer containing nickel forms a wiring having a narrow width and a short distance (for example, 30 ⁇ m or less) from the metal foil (metal foil layers 1 and 2) when the laminate is processed into a printed wiring board. Even in this case, however, it is possible to preferably prevent the migration from occurring between the wirings. Further, the nickel-containing metal particles are likely to be deposited on the base material layer so as to include needle-shaped metal particles. With the roughening treatment layer containing acicular metal particles, the anchoring effect of the F layer on the surface thereof is further improved, and the adhesiveness of the F layer to the metal foil can be sufficiently enhanced.
- the proportion of nickel atoms present on the surface of the metal foil (metal foil layer 2) is 0.03 to 0.25 mass%, preferably 0.04 to 0.2 mass%, and 0.05 to 0.15. Mass% is more preferable.
- the proportion of nickel atoms present on the surface of the metal foil (metal foil layer 2) is 0.03 to 0.25 mass%, preferably 0.04 to 0.2 mass%, and 0.05 to 0.15. Mass% is more preferable.
- the anchor effect to the surface of the F layer metal foil (metal foil layers 1 and 2) is suitably exhibited, and as a result, the adhesiveness (adhesion) of the F layer to the metal foil (metal foil layers 1 and 2).
- the average particle size of the metal particles is preferably 0.1 to 0.25 ⁇ m.
- the ten-point average roughness of the surface of the metal foil (the surface on the F layer side) is preferably 0.1 to 1.5 ⁇ m.
- 0.3 to 1.3 ⁇ m is more preferable. Further, if the ten-point average roughness is in the above range, the degree of unevenness on the surface of the metal foil is not too large, so that even if the laminate is processed into a printed wiring board, an increase in transmission loss can be suppressed.
- the ten-point average roughness of the surface of the roughening treatment layer can be adjusted by setting the size of metal particles, the number of metal particles, and the like.
- the roughening treatment layer is preferably formed by depositing (electrodeposition) metal particles on the base material layer by an electroplating method using the base material layer as a cathode.
- the electrodeposition amount such as the size of the metal particles and the number of metal particles can be controlled mainly by adjusting the current density and the electrodeposition time.
- the following plating conditions (1) or (2) are suitably used for electroplating.
- the surface of the metal foil may be subjected to a roughening treatment such as dry etching or wet etching to adjust the ten-point average roughness of the surface to the above range. Further, depending on the combination of the F polymer and the metal forming the metal foil, high adhesion between the F layer and the metal foil (metal foil layers 1 and 2) can be obtained even if the roughening treatment is omitted. Further, the metal foil may include at least one layer of a heat-resistant treatment layer, a rust-prevention treatment layer and a chromate treatment layer from the viewpoint of improving various properties.
- the metal foil has a laminated structure
- these layers are provided on the surface of the roughening treatment layer opposite to the base material layer or between the roughening treatment layer and the metal foil.
- a publicly known method can be adopted for forming the heat-resistant treatment layer, the rust-prevention treatment layer or the chromate treatment layer.
- the heat-resistant treatment layer, the rust-prevention treatment layer or the chromate treatment layer constitutes the outermost layer of the metal foil, the surface thereof constitutes the surface of the metal foil.
- the thickness of the metal foil is appropriately determined according to the application of the laminate, and when the laminate is processed into a printed wiring board and used, it is preferably 1 to 100 ⁇ m, more preferably 6 to 30 ⁇ m.
- the thickness of the ultrathin metal foil is preferably 2 to 5 ⁇ m.
- the surface of the metal foil layer 1 is formed by directly contacting the F layer on the surface of the metal foil without treating the surface of the metal foil with the silane coupling agent and forming the surface of the metal foil layer 1.
- the present laminated body 2 having the F layer provided in direct contact with the surface of the metal foil layer 2 is manufactured.
- it is preferable that the surface of the metal foil is roughened as described above, if necessary, before forming the F layer on the surface of the metal foil.
- the F layer is formed by a method of applying a dispersion liquid in which a powder of F polymer is dispersed in a solvent to the surface of the metal foil and heating, or a method of thermocompression-bonding a film containing the F polymer on the surface of the metal foil. Is preferred.
- the dispersion liquid is applied to the surface of the metal foil, and when the metal foil to which the dispersion liquid is applied is heated, the solvent is removed from the dispersion liquid and powder.
- the F layer is formed by firing and the main laminates 1 and 2 are obtained.
- the method of applying the dispersion liquid to the surface of the metal foil may be any method as long as it forms a stable liquid film (wet film) of the dispersion liquid on the surface of the metal foil, such as coating method, droplet discharge method, and dipping method.
- the coating method is preferable. By using the coating method, a liquid film can be efficiently formed on the surface of the metal foil with simple equipment.
- a coating method As a coating method, a spray method, a roll coating method, a spin coating method, a gravure coating method, a micro gravure coating method, a gravure offset method, a knife coating method, a kiss coating method, a bar coating method, a die coating method, a fountain Mayer bar method, a slot die coating.
- a spray method As a coating method, a spray method, a roll coating method, a spin coating method, a gravure coating method, a micro gravure coating method, a gravure offset method, a knife coating method, a kiss coating method, a bar coating method, a die coating method, a fountain Mayer bar method, a slot die coating.
- the metal foil to which the dispersion is applied is held at the volatilization temperature of the solvent, the dispersion is dried, and then the dried film is held at a temperature above the volatilization temperature of the solvent to bake the powder.
- the “solvent volatilization temperature” is preferably the boiling point of the solvent ⁇ 50° C., more preferably the temperature above the boiling point of the solvent, and even more preferably the temperature above the boiling point of the solvent+50° C.
- the drying temperature means the temperature of the drying atmosphere.
- the solvent does not necessarily have to be completely volatilized, and may be volatilized to such an extent that the layer shape after holding is stable.
- the amount of the solvent to be volatilized is preferably 50% by mass or more of the solvent contained in the dispersion liquid.
- the drying may be carried out in one step at a constant temperature, or in two or more steps at different temperatures.
- Examples of the drying method include a method using an oven, a method using a ventilation drying furnace, and a method of irradiating heat rays such as infrared rays. Drying may be performed under either normal pressure or reduced pressure.
- the dry atmosphere may be any of oxidizing gas atmosphere (oxygen gas etc.), reducing gas atmosphere (hydrogen gas etc.) and inert gas atmosphere (helium gas, neon gas, argon gas, nitrogen gas etc.). ..
- the drying temperature is preferably 50 to 280°C, more preferably 120 to 260°C.
- the drying time is preferably 0.1 to 30 minutes, more preferably 0.5 to 20 minutes. If the dispersion liquid is dried under the above conditions, the present laminates 1 and 2 can be preferably produced while maintaining high productivity.
- the firing method examples include a method using an oven, a method using a ventilation drying furnace, and a method of irradiating heat rays such as infrared rays.
- a firing method a method of irradiating far infrared rays is preferable because the powder can be fired in a short time and has a relatively compact size.
- the firing method may be a method combining infrared heating and hot air heating.
- the effective wavelength band of far infrared rays is preferably 2 to 20 ⁇ m, more preferably 3 to 7 ⁇ m in order to promote the uniform firing of the powder.
- the dried product of the dispersion liquid may be pressed with a heating plate, a heating roll or the like.
- the firing atmosphere may be any of an oxidizing gas atmosphere, a reducing gas atmosphere and an inert gas atmosphere. However, the firing atmosphere is preferably a reducing gas atmosphere or an inert gas atmosphere from the viewpoint of suppressing the oxidative deterioration of the metal foil and the F layer to be formed.
- the firing temperature is set according to the type of F polymer, and is preferably 180°C to 400°C, more preferably 200 to 380°C, even more preferably 220°C to 370°C.
- the firing temperature means the temperature of the firing atmosphere.
- the firing time is preferably 30 seconds to 30 minutes, more preferably 1 to 15 minutes. If the powder is fired under such conditions, the firing of the powder is promoted, the productivity of the present laminates 1 and 2 is increased, and the generation of hydrofluoric acid due to the decomposition of the F polymer is easily suppressed.
- B/A is preferably 0.1 to 1.5, more preferably 0.3 to 1.3. ..
- the specific value of D50 of the powder is preferably 0.05 to 6 ⁇ m, more preferably 0.2 to 3 ⁇ m. Within this range, the fluidity and dispersibility of the powder will be good, and the electrical properties (low dielectric constant, etc.) and heat resistance of the F layer will be most easily exhibited.
- D90 of the powder is preferably 8 ⁇ m or less, more preferably 5 ⁇ m or less.
- the loosely packed bulk density of the powder is preferably 0.05 g/mL or more, more preferably 0.08 to 0.5 g/mL.
- the dense packing bulk density of the powder is preferably 0.05 g/mL or more, more preferably 0.1 to 0.8 g/mL.
- the powder particles of the F polymer preferably consist of the F polymer. 80 mass% or more is preferable and, as for content of F polymer in a powder particle, 100 mass% is more preferable.
- Other components that may be included in the powder particles include aromatic polyester, polyamideimide, thermoplastic polyimide, polyphenylene ether, and polyphenylene oxide.
- the solvent in the dispersion liquid is a compound that is liquid at 25° C., and may be an aqueous solvent or a non-aqueous solvent.
- the solvent is preferably water, amide, alcohol, sulfoxide, ester, ketone or glycol ether, more preferably water, ketone or amide, still more preferably ketone or amide.
- As the solvent one type may be used alone, or two or more types may be used in combination.
- the solvent include water, methanol, ethanol, isopropanol, N,N-dimethylformamide, N,N-dimethylacetamide, N-methyl-2-pyrrolidone, dimethyl sulfoxide, diethyl ether, dioxane, ethyl lactate, ethyl acetate. , Butyl acetate, methyl ethyl ketone, methyl isopropyl ketone, cyclopentanone, cyclohexanone, ethylene glycol monoisopropyl ether, cellosolve (methyl cellosolve, ethyl cellosolve, etc.).
- the solvent is a polar solvent from the viewpoint of increasing the wettability between the surface of the metal foil and the F polymer and allowing the hydroxyl group and/or the metal atom on the surface of the metal foil and the oxygen-containing polar group of the F polymer to interact better.
- a polar solvent from the viewpoint of increasing the wettability between the surface of the metal foil and the F polymer and allowing the hydroxyl group and/or the metal atom on the surface of the metal foil and the oxygen-containing polar group of the F polymer to interact better.
- water, amide or ketone is preferred, and water, N,N-dimethylacetamide, N-methyl-2-pyrrolidone, cyclohexanone or methyl ethyl ketone is more preferred.
- the dispersion preferably further contains a fluorine-based dispersant.
- the fluorinated dispersant is a compound having a function of chemically and/or physically adsorbing on the surface of the powder particles to stably disperse the powder particles in a solvent.
- the dispersibility of the powder is further improved, the wettability between the surface of the metal foil and the F polymer is increased, and the oxide and/or metal atom and the F polymer on the surface of the metal foil are dispersed. Highly likely to interact with the oxygen-containing polar group possessed.
- the fluorine-based dispersant is preferably a compound (surfactant) having a hydrophobic moiety containing a fluorine atom and a hydrophilic moiety, more preferably fluoropolyol, fluorosilicone or fluoropolyether, and further preferably fluoropolyol.
- the fluorine-based dispersant is preferably a nonionic polymeric compound. Such a fluorine-based dispersant has a high interaction with the above-mentioned solvent, and thus the coating film-forming properties (thixo ratio, adhesiveness, transparency, etc.) of the dispersion liquid are easily improved.
- Fluoropolyol unlike F polymer, is a polymeric polyol having a hydroxyl group and a fluorine atom. Further, in the polymeric polyol, a part of hydroxyl groups may be chemically modified and modified. Examples of the fluoropolyol include compounds having a main chain composed of a carbon chain derived from an ethylenically unsaturated monomer and a side chain branched from the main chain having a fluorine-containing hydrocarbon group and a hydroxyl group.
- the decomposition product of the fluoropolyol when the dispersion is applied and heated easily forms an oxide on the surface of the metal foil, and the metal foil (metal foil layers 1 and 2) And the polymer layer can be more firmly adhered.
- Fluoropolyol is a copolymer containing a unit based on a fluorine-containing (meth)acrylate having a polyfluoroalkyl group or a polyfluoroalkenyl group and a unit based on a hydrophilic (meth)acrylate having a polyoxyalkylene group or a hydroxyalkyl group.
- (meth)acrylate is a general term for acrylate derivatives in which the hydrogen atom at the ⁇ -position of acrylate, methacrylate and acrylate is substituted with another atom or atomic group.
- fluorine-containing (meth)acrylate examples include CH 2 ⁇ CHCOO(CH 2 ) 2 (CF 2 ) 4 F, CH 2 ⁇ C(CH 3 )COO(CH 2 ) 2 (CF 2 ) 4 F, CH.
- the fluoropolyol may contain only a unit based on a fluorine-containing (meth)acrylate and a unit based on a hydrophilic (meth)acrylate, and may further contain another unit.
- the fluorine content of the fluoropolyol is preferably 10 to 45% by mass, more preferably 15 to 40% by mass.
- the weight average molecular weight of the fluoropolyol is preferably 2,000 to 80,000, more preferably 6,000 to 20,000.
- fluorosilicone examples include polyorganosiloxane containing a C—F bond in a part of the side chain.
- fluoropolyether examples include compounds in which a part of hydrogen atoms of polyoxyalkylene alkyl ether is substituted with fluorine atoms.
- the fluoropolyether also includes monool compounds of the above compounds.
- the dispersion may contain other materials. Other materials may or may not dissolve in the dispersion. Such other material may be a non-curable resin or a curable resin.
- the non-curable resin include a heat-meltable resin and a non-meltable resin.
- the heat-meltable resin include thermoplastic polyimide.
- the non-melting resin include a cured product of a curable resin.
- the curable resin examples include a polymer having a reactive group, an oligomer having a reactive group, a low molecular compound, and a low molecular compound having a reactive group.
- the reactive group include a carbonyl group-containing group, a hydroxy group, an amino group and an epoxy group.
- the curable resin is an epoxy resin, a thermosetting polyimide, a polyimide precursor polyamic acid, an acrylic resin, a phenol resin, a polyester resin, a polyolefin resin, a modified polyphenylene ether resin, a polyfunctional cyanate ester resin, a polyfunctional maleimide-cyan.
- Examples thereof include acid ester resins, polyfunctional maleimide resins, vinyl ester resins, urea resins, diallyl phthalate resins, melanin resins, guanamine resins, and melamine-urea co-condensation resins.
- epoxy resin examples include various types of epoxy resins (naphthalene type, cresol novolac type, bisphenol A type, bisphenol F type, bisphenol S type, alicyclic type, aliphatic chain type, cresol novolac type, phenol novolac type). Type, alkylphenol novolac type, aralkyl type, biphenol type, etc.).
- bismaleimide resin examples include the resin composition (BT resin) described in JP-A-7-70315 and the resin described in International Publication No. 2013/008667.
- the polyamic acid usually has a reactive group capable of reacting with the oxygen-containing polar group of the F polymer.
- Examples of diamines and polycarboxylic acid dianhydrides that form polyamic acids include [0020] in Japanese Patent No. 5766125, [0019] in Japanese Patent No. 5766125, and [0055] in Japanese Patent Application Laid-Open No. 2012-145676, [0057] and the like.
- thermoplastic resins such as thermoplastic polyimide and heat-curable cured products of curable resins.
- thermoplastic resin polyester resin, polyolefin resin, styrene resin, polycarbonate, thermoplastic polyimide, polyarylate, polysulfone, polyallylsulfone, aromatic polyamide, aromatic polyetheramide, polyphenylene sulfide, polyallyl ether ketone, polyamide
- imide liquid crystalline polyester and polyphenylene ether
- thermoplastic polyimide liquid crystalline polyester or polyphenylene ether are preferable.
- Such other materials include thixotropic agents, antifoaming agents, inorganic fillers, reactive alkoxysilanes, dehydrating agents, plasticizers, weathering agents, antioxidants, heat stabilizers, lubricants, antistatic agents, and additives.
- a whitening agent, a coloring agent, a conductive agent, a release agent, a surface treatment agent, a viscosity modifier, and a flame retardant are also included.
- the viscosity of the dispersion liquid is preferably 50 to 10000 mPa ⁇ s, more preferably 75 to 1000 mPa ⁇ s, and further preferably 100 to 500 mPa ⁇ s. In this case, not only is the dispersibility of the dispersion liquid excellent, but also its coatability and compatibility with varnishes of different resin materials are excellent.
- the thixo ratio of the dispersion is preferably 1.0 to 2.2, more preferably 1.4 to 2.2, and even more preferably 1.5 to 2.0. In this case, not only the dispersibility of the dispersion liquid is excellent, but also the homogeneity of the F layer is likely to be improved.
- the thixo ratio is calculated by dividing the viscosity of the dispersion liquid measured under the condition of the rotation speed of 30 rpm by the viscosity of the dispersion liquid measured under the condition of the rotation speed of 60 rpm.
- the film containing the F polymer in the method of thermocompression-bonding the film containing the F polymer on the surface of the metal foil, when the film containing the F polymer is thermocompression bonded to the surface of the metal foil, the F layer is formed, and the metal foil layer 1 and the metal foil layer 1 composed of the metal foil are formed.
- the main laminates 1 and 2 having the F layer provided in direct contact with the surface of 2 are obtained.
- the film can be produced by a method of molding the F polymer itself or a composition containing the F polymer into a film by an extrusion molding method, an inflation molding method, or the like.
- the laminated body is manufactured by a preliminary heating step in which a temporary laminated body in which a film is laminated on the surface of a metal foil is heated without being pressed in the thickness direction (laminating direction) while being transported, and a temporary laminated body. It is performed through a thermocompression bonding step in which the body is heated and pressed in the thickness direction (laminating direction) to be bonded.
- the temporary laminate the metal foil and the film are in close contact with each other, but are in a state where they are not yet adhered (pressed).
- the film Before forming the temporary laminate, the film may be preliminarily heat-treated at a temperature of 100°C or higher and lower than 250°C (preferably 180°C or higher and lower than 250°C). If heat treatment is performed in advance, the shrinkage of the film in the preheating step and the thermocompression bonding step can be reduced, and as a result, the warpage of the laminate can be reduced.
- the surface of the film (the surface on the metal foil side) may be subjected to surface treatment such as corona discharge treatment and plasma treatment. If the surface treatment is performed in advance, the number of oxygen-containing polar groups existing on the surface of the film can be increased, and in the resulting laminate, the adhesive strength of the F layer to the metal foil layers 1 and 2 can be further increased.
- the temporary laminate is heated by the preliminary heating means without being pressed in the laminating direction (thickness direction) before being pressure-bonded in the subsequent thermocompression bonding step.
- the preheating means may be a contact method in which a heat source is brought into contact with the temporary laminate or a non-contact method in which the temporary laminate is heated in a non-contact manner.
- the contact method is preferable as the preheating means because the metal foil and the film are easily attached to each other. Specifically, a method of transporting the temporary laminated body in contact with a heated metal roll is preferable.
- the temperature (temporary heating temperature) of the temporary laminate immediately before being pressed in the thermocompression bonding step is preferably 20° C.
- the preheating temperature is preferably equal to or lower than the thermocompression bonding temperature. When the preheating temperature is within the above range, shrinkage and breakage of the film can be favorably prevented.
- the temporary laminate may be heated continuously or intermittently.
- the transportation time (preheating time) from the position where preheating is started to the temporary laminate being transported to immediately before the temporary lamination is pressed in the thermocompression bonding step is preferably 10 to 30 seconds.
- the preheating time is within the above range, the adhesive force of the F layer to the metal foil layers 1 and 2 is increased in the obtained laminate while satisfactorily preventing the film from shrinking or breaking.
- the preheating step is performed by the contact type preheating means, if the preheating time is in the above range, the temperature of the temporary laminate becomes the same temperature as the surface temperature of the heat source brought into contact with the temporary laminate.
- thermocompression bonding process is preferably performed continuously using a thermocompression bonding device or the like equipped with one or more thermocompression bonding means.
- the thermocompression bonding means means that press-bonds by pressing the temporary laminate while heating it.
- a heat roll pressure bonding device having a pair of metal rolls is preferably used as the heat pressure bonding means.
- the temporary laminate is heated by contact with the metal roll when passing between the pair of metal rolls heated to a predetermined temperature, and receives a pressing force in the thickness direction.
- the film is crimped to the metal foil.
- the temporary laminated body may pass through a plurality of pairs of metal rolls in order.
- the surface temperature (temperature of thermocompression bonding) of the metal roll that pressurizes the temporary laminate is preferably the melting temperature of the F polymer or higher, and more preferably 400° C. or higher. In this case, good adhesive strength of the F layer to the metal foil layers 1 and 2 is obtained, and peeling is less likely to occur.
- the pressure between the pair of metal rolls (pressure for thermocompression bonding) that pressurizes the temporary laminate is a roll linear pressure represented by a load applied per 1 cm width of the roll, and is preferably 98 to 1470 N/cm. In this case, the film does not easily break during thermocompression bonding, good adhesive strength of the F layer to the metal foil layers 1 and 2 is obtained, and peeling hardly occurs.
- the traveling speed (speed of thermocompression bonding) when the temporary laminate passes between a pair of metal rolls is preferably 0.5 m/min or more, more preferably 1 m/min or more. In this case, thermocompression bonding can be sufficiently performed, and the productivity of the main laminates 1 and 2 can be further improved.
- the speed of thermocompression bonding is preferably 8 m/min or less. In this case, the F layer and the metal foil layers 1 and 2 can be easily adhered firmly.
- the film may be a laminated film having a heat resistant resin film on the surface of the film (base film) containing the F polymer opposite to the metal foil.
- the heat resistant resin film contains a heat resistant resin, and may contain additives and the like as necessary. From the viewpoint of increasing the heat resistance of the heat-resistant resin film, the content of the heat-resistant resin in the heat-resistant resin film is preferably 50% by mass or more, more preferably 80% by mass or more.
- thermosetting resin As the heat resistant resin, polyimide (aromatic polyimide etc.), polyarylate, polysulfone, polyallyl sulfone (polyether sulfone etc.), aromatic polyamide, aromatic polyether amide, polyphenylene sulfide, polyallyl ether ketone, polyamide imide , And liquid crystal polyester.
- the heat-resistant resin is preferably a thermosetting resin because it is easy to obtain higher heat resistance.
- thermosetting resin include thermosetting polyimide, epoxy resin, and acrylic resin. From the viewpoint of improving the electrical characteristics of the laminate, the thermosetting resin is preferably thermosetting polyimide.
- aromatic polyimide is preferable, and wholly aromatic polyimide produced by polycondensation of aromatic dicarboxylic acid and aromatic diamine is more preferable.
- an inorganic filler having a low relative dielectric constant and a low dielectric loss tangent is preferable.
- Such inorganic fillers include silica, clay, talc, calcium carbonate, mica, diatomaceous earth, alumina, zinc oxide, titanium oxide, calcium oxide, magnesium oxide, iron oxide, tin oxide, antimony oxide, calcium hydroxide, magnesium hydroxide, Aluminum hydroxide, basic magnesium carbonate, magnesium carbonate, zinc carbonate, barium carbonate, dawsonite, hydrotalcite, calcium sulfate, barium sulfate, calcium silicate, montmorillonite, bentonite, activated clay, sepiolite, imogolite, sericite, glass fiber, Examples thereof include glass beads, silica-based balloons, carbon black, carbon nanotubes, carbon nanohorns, graphite, carbon fibers, glass balloons, carbon burns, wood powder, and zinc borate.
- the inorganic fillers may be used alone or in combination of two or more.
- the peel strength of the F layer from the metal foil layers 1 and 2 is preferably 10 N/cm or more, more preferably 15 N/cm or more.
- the upper limit of the peel strength is usually 20 N/cm.
- the warpage rate of the present laminates 1 and 2 is preferably 25% or less, more preferably 7% or less. In this case, the handleability when processing the laminated bodies 1 and 2 into a printed wiring board and the transmission characteristics of the obtained printed wiring board are excellent.
- the dimensional change rate of the laminates 1 and 2 is preferably ⁇ 1% or less, more preferably ⁇ 0.2% or less. In this case, it is easy to process the laminated bodies 1 and 2 into a printed wiring board and further form a multilayered structure.
- the water contact angle of the surface of the F layer is preferably 70 to 100°, more preferably 70 to 90°. In this case, the adhesiveness between the F layer and another substrate is more excellent.
- the thickness of the F layer is preferably 1 to 50 ⁇ m, more preferably 5 to 15 ⁇ m. Within this range, it is easy to balance the electrical characteristics and the warp suppressing effect of the laminate when the laminates 1 and 2 are processed into a printed wiring board.
- the composition and thickness of each F layer are, respectively, from the viewpoint of suppressing warpage of the laminates 1 and 2. It is preferably the same.
- the relative permittivity of the F layer is preferably 1.98 or less, more preferably 1.95 or less.
- the lower limit of the relative dielectric constant of the F layer is usually 1.50.
- the dielectric loss tangent of the F layer is preferably 0.0024 or less, more preferably 0.0019 or less.
- the lower limit of the relative dielectric constant of the F layer is usually 0.0005.
- the present laminates 1 and 2 can be preferably used for a printed wiring board or the like which is required to have a low dielectric constant.
- the relative dielectric constant and dielectric loss tangent of the F layer are values measured at a measurement frequency of 10 GHz by a cavity resonator perturbation method using a network analyzer as a measuring instrument.
- the laminates 1 and 2 can be processed into a printed wiring board.
- an interlayer insulating film may be formed on the pattern circuit, and a conductor circuit may be further formed on the interlayer insulating film.
- the interlayer insulating film may be formed from the above dispersion liquid.
- a solder resist may be laminated on the pattern circuit.
- the solder resist may be formed from the above dispersion liquid.
- a coverlay film may be laminated on the pattern circuit.
- the coverlay film may be formed from the above dispersion liquid.
- the method for producing a composite laminate (present composite) of the present invention comprises removing at least a part of a metal foil layer of a predetermined laminate (metal layer with F layer), adhering a prepreg to an exposed polymer layer, It is a method for obtaining a composite laminate in which at least a polymer layer and a prepreg layer are laminated.
- a two-layer composite laminate having a polymer layer and a prepreg layer can be obtained.
- a part of the metal foil layer to form a circuit pattern a three-layer composite laminate having a polymer layer, a prepreg layer, and a circuit pattern sandwiched between them can be obtained.
- the latter composite laminate can be suitably used as a printed wiring board.
- the laminate used for producing the composite laminate includes a metal foil layer having a surface having a ten-point average roughness of 0.1 ⁇ m or more, and an F layer laminated on the surface.
- the surface of the metal foil layer has a ten-point average roughness of 0.1 ⁇ m or more, and minute irregularities are irregularly present.
- the F layer formed on this surface has the surface shape of the metal foil layer transferred to the contact surface with the metal foil layer. Therefore, on the contact surface of the F layer exposed by the removal of the metal foil layer, minute irregularities corresponding to the surface shape of the metal foil layer are irregularly present.
- a prepreg is adhered to the contact surface having such a surface texture to obtain a composite laminate, it is considered that a high anchoring effect for the contact surface of the F layer of the prepreg is produced. As a result, it is presumed that a high adhesive force (peeling strength) was developed between the F layer and the prepreg layer. The effects as described above are remarkably exhibited in a preferred embodiment of the present invention described later.
- the aspect of the F polymer in the method for producing the present composite body is the same as that of the F polymer in the present laminate body including the preferable aspect.
- Aspects of the metal constituting the metal foil layer in the method for producing the present composite body are the same as those of the metal constituting the metal foil layer in the present laminate including suitable aspects.
- the ten-point average roughness of the surface of the metal foil layer in the method for producing this composite is 0.1 ⁇ m or more, preferably 0.3 ⁇ m or more.
- the ten-point average roughness is preferably 7 ⁇ m or less, more preferably 2.5 ⁇ m or less, still more preferably 2 ⁇ m or less. Further, if the ten-point average roughness is in the above range, the degree of unevenness on the surface of the metal foil layer is not too large, so that even if the present composite is processed into a printed wiring board, an increase in transmission loss can be suppressed.
- the matrix resin of the prepreg and the F polymer are compatibilized, and the adhesive force between the layers is more likely to be improved.
- the ten-point average roughness of the surface can be adjusted by setting the size of metal particles, the number of metal particles, and the like.
- the roughening treatment layer is preferably formed by depositing (electrodeposition) metal particles on the base material layer by an electroplating method using the base material layer as a cathode.
- the electrodeposition amount such as the size of the metal particles and the number of metal particles can be controlled mainly by adjusting the current density and the electrodeposition time.
- the conditions for electroplating can be the same as the conditions for electroplating in the laminate.
- the surface of the metal foil layer may be subjected to a roughening treatment such as dry etching or wet etching to adjust the ten-point average roughness of the surface within the above range.
- the metal foil layer may include at least one layer selected from a heat-resistant treatment layer, a rust-prevention treatment layer and a chromate treatment layer from the viewpoint of improving various properties.
- these layers are provided on the surface of the roughening treatment layer opposite to the base material layer or between the roughening treatment layer and the metal foil.
- a publicly known method can be adopted for forming the heat-resistant treatment layer, the rust-prevention treatment layer or the chromate treatment layer.
- the heat-resistant treatment layer, the rust-prevention treatment layer or the chromate treatment layer constitutes the outermost layer of the metal foil layer
- the surface thereof constitutes the surface of the metal foil layer.
- the thickness of the metal foil layer the same conditions as the thickness of the metal foil layer of the present laminate can be adopted.
- the aspect of the F layer in the method for producing the present composite body is the same as that in the present laminate body, including its preferable aspect and its forming method.
- the removal of the metal foil layer in the method for producing the present composite body is preferably performed by wet etching.
- wet etching unnecessary portions of the metal foil layer can be accurately and sufficiently removed while preventing damage to the minute uneven shape transferred to the contact surface of the F layer.
- wet etching is preferably performed using an acid solution.
- the F polymer has a hydrolyzable acid anhydride residue as the oxygen-containing polar group
- the oxygen-containing polar group is activated by the acid solution, the adhesive force of the F layer with the prepreg layer is likely to be further increased.
- activation of the oxygen-containing polar group conversion of an acid anhydride group into a 1,2-dicarboxylic acid group can be mentioned.
- the acid solution an aqueous solution of an inorganic acid such as hydrochloric acid, dilute nitric acid or hydrofluoric acid can be used.
- a prepreg is a sheet-shaped substrate in which a matrix resin is impregnated into a base material (tow, woven cloth, etc.) of reinforcing fibers (glass fiber, carbon fiber, etc.).
- the matrix resin may be a thermoplastic resin or a thermosetting resin. That is, the prepreg layer is a layer formed from the prepreg.
- the prepreg layer is a layer containing a cured product of the matrix resin if the matrix resin is curable, and a layer containing a melted and solidified product of the matrix resin if the matrix resin is thermoplastic.
- thermosetting resin examples include the resins described in the description of the above-mentioned dispersion liquid, and an epoxy resin, polyphenylene oxide, polyphenylene ether, or polybutadiene is preferable.
- the polyphenylene ether is preferably a modified polyphenylene ether, more preferably a vinyl group-containing polyphenylene ether.
- thermoplastic resin examples include the resins mentioned in the description of the dispersion liquid.
- the matrix resin one type may be used alone, or two or more types may be used in combination.
- the matrix resin of the prepreg is preferably an epoxy resin, polyphenylene oxide, polyphenylene ether or polybutadiene from the viewpoint of workability.
- the prepreg preferably contains a curing agent, and contains a curing agent having three or more curable groups (isocyanate group, blocked isocyanate group, etc.) in one molecule. Hardeners are more preferred.
- a resin having a fluorine atom may be used as the matrix resin. Examples of such resin include F polymer, polyimide having a fluorine atom, and epoxy resin having a fluorine atom.
- Preferable embodiments of the matrix resin include an embodiment composed only of a matrix resin having no fluorine atom, and an embodiment composed of a matrix resin having no fluorine atom and a matrix resin having a fluorine atom.
- the reinforcing fiber sheet includes a reinforcing fiber bundle composed of a plurality of reinforcing fibers, a cloth woven from the reinforcing fiber bundle, a unidirectional reinforcing fiber bundle in which a plurality of reinforcing fibers are aligned in one direction, and the unidirectional reinforcing fiber.
- a unidirectional cloth composed of a bundle or a combination of these, and a laminate of a plurality of reinforcing fiber bundles.
- the reinforcing fibers continuous long fibers having a length of 10 mm or more are preferable.
- the reinforcing fibers do not need to be continuous over the entire length of the reinforcing fiber sheet in the length direction or the entire width in the width direction, and may be divided in the middle.
- the reinforcing fiber may be subjected to a surface treatment such as a silane coupling agent treatment.
- Examples of the reinforcing fiber include inorganic fiber, metal fiber, organic fiber and the like.
- Examples of the inorganic fiber include carbon fiber, graphite fiber, glass fiber, silicon carbide fiber, silicon nitride fiber, alumina fiber, silicon carbide fiber, boron fiber and the like.
- Examples of the metal fibers include aluminum fibers, brass fibers, stainless fibers and the like.
- Examples of the organic fibers include aromatic polyamide fibers, polyaramid fibers, polyparaphenylenebenzoxazole (PBO) fibers, polyphenylene sulfide fibers, polyester fibers, acrylic fibers, nylon fibers, polyethylene fibers and the like.
- the reinforcing fibers may be used alone or in combination of two or more.
- the glass fiber is preferable as the reinforcing fiber in the printed circuit board material application.
- the method of adhering the prepreg to the F layer is preferably a method of bringing the prepreg into contact with the contact surface of the F layer in which at least a part of the laminate is exposed, and thermocompression bonding.
- the temperature for thermocompression bonding is preferably not higher than the melting temperature of the F polymer, more preferably 120 to 300°C, and even more preferably 160 to 220°C. Within this range, the polymer layer and the prepreg layer can be firmly bonded while suppressing the thermal deterioration of the prepreg.
- the pressure for thermocompression bonding is preferably 0.2 MPa or more.
- the pressure is preferably 10 MPa or less, more preferably 4 MPa or less.
- the F layer and the prepreg layer can be more firmly bonded while suppressing damage to the prepreg. Furthermore, when the prepreg is thermocompression bonded to the contact surface of the F layer at such heat temperature or pressure bonding, the prepreg layer that has entered the F layer due to the anchor effect and the F polymer are more compatible and integrated, The adhesive strength is easier to improve.
- thermocompression bonding is preferably performed in a reduced pressure atmosphere, more preferably at a vacuum degree of 20 kPa or less. Within this range, it is possible to prevent bubbles from being mixed into the interface between the F layer and the prepreg layer, and suppress deterioration of the present composite due to oxidation. Further, during hot pressing, it is preferable to raise the temperature after reaching the above vacuum degree. In this way, since the F layer is pressure-bonded before being softened, that is, before a certain degree of fluidity and adhesiveness is developed, it is possible to prevent the generation of bubbles.
- the exposed surface of the F layer is subjected to a hydrophilic treatment.
- the F layer can be directly adhered to the prepreg layer without doing so.
- the hydrophilic treatment is a treatment for reducing the contact angle of water with respect to the exposed surface of the F layer, and specific examples thereof include plasma treatment, ionizing radiation treatment, and treatment with a silane coupling agent.
- the peel strength of the F layer from the prepreg layer is preferably 10 N/cm or more, more preferably 15 N/cm or more.
- the upper limit of the peel strength is usually 20 N/cm.
- the warpage rate of the present composite body is preferably 25% or less, more preferably 7% or less. In this case, the transmission characteristics of this composite (printed wiring board) are excellent.
- the dimensional change rate of the composite is preferably ⁇ 1% or less, more preferably ⁇ 0.2% or less. In this case, it is easy to make the composite into multiple layers.
- a processed laminate obtained by removing a part of the metal foil layer of the laminate and forming a metal circuit layer (circuit pattern) from the metal foil layer is a printed circuit having excellent solder reflow resistance. It is useful as a substrate.
- a multilayer printed circuit board having such a multilayer structure of the printed circuit board and having an F layer as the outermost layer is excellent in heat resistance, and specifically, even at 288° C., the prepreg layer has an interface at the interface. Swelling and peeling at the interface of the metal circuit layer are less likely to occur.
- the F layer has a predetermined thickness (1 to 15 ⁇ m, particularly 3 to 9 ⁇ m), this tendency tends to be remarkable.
- a multilayer printed circuit board having such a multilayer structure of the printed circuit board and having a prepreg layer as the outermost layer is also excellent in heat resistance, and specifically, even at 300° C., the prepreg layer has an interface at the interface. Swelling and peeling at the interface of the metal circuit layer are less likely to occur.
- the F layer has a predetermined thickness (1 to 15 ⁇ m, particularly 3 to 9 ⁇ m), this tendency tends to be remarkable.
- the metal of a laminate having a metal foil layer having a surface having a ten-point average roughness of 0.1 ⁇ m or more and an F layer laminated on the surface.
- a method for producing a laminate in which at least a part of a foil is removed, a solder resist is applied to the exposed F layer and cured to form a solder mask layer, and at least the F layer and the solder mask layer are laminated. It The mode of removing at least a part of the metal foil (metal foil layer), the F polymer, the F layer, the laminated body, and the metallic foil layer of the laminated body in this manufacturing method includes the preferable range of the present composite body. It is similar to those of the manufacturing method.
- solder resist A publicly known solder resist can be used as the solder resist. Further, the application and curing of the solder resist may be appropriately determined according to the type of solder resist used. In this manufacturing method, it is preferable that the surface of the exposed F layer is treated with an acid solution and the solder resist is directly applied and cured as it is. In this case, in the formation of the solder mask layer, it is easier to form the solder mask layer having more excellent adhesion as compared with the case where the surface treatment (buffing) is performed after the acid treatment.
- all the metal foil layers of the above-mentioned laminate can be removed and the remaining single F layer can be used as a polymer film.
- a polymer film can be used as an adhesive layer for adhering two substrates, an interlayer insulating film, a solder resist layer, a coverlay film, or the like.
- the laminate and the method for producing the same, the method for producing the composite laminate, and the method for producing the polymer film of the present invention have been described above, but the present invention is not limited to the configurations of the above-described embodiments.
- the laminate of the present invention may have any other configuration added to the configuration of the above-described embodiment, or may be replaced with any configuration exhibiting the same function.
- the method for producing a laminate of the present invention, the method for producing a composite laminate, and the method for producing a polymer film, respectively, in the configuration of the above-described embodiment, other optional steps may be added, the same. It may be replaced with any step that exerts the function of.
- F polymer 1 a copolymer containing 98.0 mol%, 0.1 mol% and 1.9 mol% of units based on TFE, units based on NAH and units based on PPVE in this order (melting temperature: 300° C., 380° C.
- F polymer 2 a copolymer containing 98.0 mol% and 2.0 mol% of units based on TFE and units based on PPVE in this order and having no oxygen-containing polar group (melting temperature: melting at 305° C., 380° C. Viscosity: 3 ⁇ 10 5 Pa ⁇ s)
- F polymer 3 a copolymer having no functional group, containing 97.5 mol% and 2.5 mol% of units based on TFE and units based on PPVE in this order (melting temperature: 305° C., melt viscosity at 380° C.: 3 ⁇ 10 5 Pa ⁇ s)
- Powder 1 Powder composed of F polymer 1 (D50: 2.6 ⁇ m, D90: 7.1 ⁇ m)
- Powder 2 Powder composed of F polymer 2 (D50: 3.5 ⁇ m, D90: 9.2 ⁇ m)
- Powder 3 Powder composed of F polymer 2 (D50: 1.8 ⁇ m, D90: 4.9 ⁇ m)
- Powder 4 Powder composed of F polymer 1 (D50: 1.8 ⁇ m, D90: 5.2 ⁇ m)
- Powder 5 Powder composed of F polymer 3 (D50: 1.9 ⁇ m, D90: 5.5 ⁇ m)
- D50 and D90 were measured by dispersing the powder in water using a laser diffraction/scattering type particle size distribution measuring device (LA-920 measuring device manufactured by Horiba Ltd.).
- [Fluorine-based dispersant] FP1 CH 2 ⁇ CHCOO(CH 2 ) 4 OCF(CF 3 )(C(CF(CF 3 ) 2 )( ⁇ C(CF 3 ) 2 ) and CH 2 ⁇ CHCOO(CH), which are nonionic fluoropolyols. 2 ) 4 (OCH 2 CH 2 ) 10 OH copolymer [sheet] Sheet 1: Sheet made of F polymer 1 (thickness: 10 ⁇ m) Sheet 2: Sheet made of F polymer 3 (thickness: 10 ⁇ m) [Prepreg] Prepreg 1: Thermosetting resin composition containing polyphenylene ether resin, glass fiber and silica filler
- Dispersion 1 After 47 parts by mass of N-methyl-2-pyrrolidone (NMP), 2.5 parts by mass of FP1 and 50 parts by mass of powder 1 were put into a pot, zirconia balls were put into the pot. Then, the pot was rolled at 150 rpm for 1 hour to disperse the powder 1 in NMP to prepare a dispersion 1. (Dispersion liquid 2) Dispersion 2 was prepared in the same manner as Dispersion 1 except that Powder 1 was changed to Powder 2.
- NMP N-methyl-2-pyrrolidone
- Dispersion liquid 2 Dispersion 2 was prepared in the same manner as Dispersion 1 except that Powder 1 was changed to Powder 2.
- Dispersion 3 Dispersion 3 was prepared in the same manner as Dispersion 1 except that Powder 1 was changed to Powder 3.
- Dispersion liquid 4 was prepared in the same manner as dispersion liquid 1 except that powder 1 was changed to powder 4 and the amount of FP1 was changed to 3 parts by mass.
- Dispersion 5 was prepared in the same manner as Dispersion 1 except that Powder 1 was changed to Powder 5 and the amount of FP1 was changed to 3 parts by mass.
- metal foil 1 Using a rolled copper foil (base material layer) having a thickness of 12 ⁇ m as a cathode, electroplating was performed under the following conditions to form a roughening treatment layer on the surface of the rolled copper foil. Thereby, the metal foil 1 was produced. Then, a heat-resistant treatment layer and a chromate layer were sequentially formed on the surface of the roughening treatment layer.
- the thickness of the metal foil 1 was 15 ⁇ m, and the ten-point average roughness of the surface was 0.6 ⁇ m.
- ⁇ Primary particle plating (1)> Liquid composition: Copper sulfate pentahydrate 11 g/L, sulfuric acid 52 g/L Liquid temperature: 22°C Current density: 40 A/dm 2 Electrodeposition time: 1 second ⁇ Primary particle plating (2)> Liquid composition: Copper sulfate pentahydrate 19 g/L, sulfuric acid 101 g/L Liquid temperature: 42°C Current density: 4 A/dm 2 Electrodeposition time: 3 seconds ⁇ Secondary particle plating> Liquid composition: Copper sulfate pentahydrate 15 g/L, nickel sulfate hexahydrate 10 g/L , Cobalt sulfate heptahydrate 7g/L Liquid temperature: 37°C Current density: 30 A/dm 2 Electrodeposition time: 1 second
- Metal foil 2 On the surface of the metal foil 1, a solution containing a silane coupling agent (“KBM series” manufactured by Shin-Etsu Chemical Co., Ltd.) in an amount of 1% by volume was used and subjected to surface treatment under the following conditions to prepare a metal foil 2.
- the thickness of the metal foil 2 was 15 ⁇ m, and the ten-point average roughness of the surface was 0.6 ⁇ m.
- Metal foil 3 Using titanium coated with a white metal oxide as an anode, and using an electrolytic copper foil having a ten-point average roughness (Rzjis) of 0.75 ⁇ m and a thickness of 12 ⁇ m as a cathode, electroplating was performed under the following conditions. A roughening treatment layer was formed on the surface of the electrolytic copper foil to prepare a metal foil 3.
- Rzjis ten-point average roughness
- Metal foil 4 was produced in the same manner as the metal foil 3 except that the liquid composition shown below was changed.
- Liquid composition copper sulfate pentahydrate 15 g/L, cobalt sulfate heptahydrate 8.5 g/L
- the ten-point average roughness of the surface of the metal foil 4 was 1.0 ⁇ m.
- the proportion of nickel atoms existing on the surface of the metal foil 4 (roughening treatment layer) measured in the same manner as above was 0.00% by mass.
- Metal foil 5 A metal foil 5 was produced in the same manner as the metal foil 3 except that the liquid composition shown below was changed.
- Liquid composition copper sulfate pentahydrate 15 g/L, cobalt sulfate heptahydrate 8.5 g/L , Nickel sulfate hexahydrate 8.6 g/L
- the ten-point average roughness of the surface of the metal foil 5 was 1.0 ⁇ m. Further, the proportion of nickel atoms present on the surface of the metal foil 5 (roughening treatment layer) measured in the same manner as above was 0.30 mass %.
- Metal foil 6 After electroplating the electrolytic copper foil to form a roughening treatment layer, a heat-resistant treatment layer and a chromate layer were sequentially formed on the roughening treatment layer to produce a metal foil 6.
- the ten-point average roughness of the surface of the metal foil 6 was 0.2 ⁇ m, and the thickness was 12 ⁇ m.
- Metal foil 7 A metal foil 7 was manufactured in the same manner as the metal foil 6.
- the ten-point average roughness of the surface of the metal foil 7 was 1.2 ⁇ m, and the thickness was 18 ⁇ m.
- Metal foil 8 A metal foil 8 was manufactured in the same manner as the metal foil 6.
- the ten-point average roughness of the surface of the metal foil 8 was 7.7 ⁇ m, and the thickness was 18 ⁇ m.
- the liquid dispersion 1 was formed by coating the surface of the metal foil 1 with the dispersion liquid 1 by roll-to-roll by die coating.
- the metal foil 1 on which this liquid film was formed was passed through a drying oven at 120° C. for 30 minutes and dried by heating. The dry coating was then heated at 380°C for 15 minutes in a nitrogen oven. In this way, the laminated body 1 in which the F layer was formed on the surface of the metal foil 1 was manufactured.
- Example 2 (comparative example) A laminate 2 was produced in the same manner as in Example 1 except that the metal foil 1 was changed to the metal foil 2.
- Example 3 (comparative example) A laminate 3 was produced in the same manner as in Example 1 except that the dispersion liquid 1 was changed to the dispersion liquid 2.
- Example 4 A laminate 4 having an F layer thickness of 12 ⁇ m was produced in the same manner as in Example 1 except that the metal foil 1 was changed to the metal foil 3. Using two sheets of this laminate 4 and one sheet of a polyimide film (thickness: 25 ⁇ m; Ube Industries, Ltd., “Upilex 25S”), apply the F layer of each laminate 1 to both sides of the polyimide film. And laminated by heating at 360° C. to further produce a laminate 41 having metal foil layers on both outermost surfaces.
- Example 5 A laminate 5 and a laminate 51 each having an F layer thickness of 12 ⁇ m were manufactured in the same manner as in Example 4 except that the metal foil 3 was changed to the metal foil 4.
- Example 6 A laminate 6 and a laminate 61 each having an F layer thickness of 12 ⁇ m were manufactured in the same manner as in Example 4 except that the metal foil 3 was changed to the metal foil 5.
- Example 7 A laminate 7 having an F layer thickness of 12 ⁇ m was produced in the same manner as in Example 4 except that the dispersion liquid 1 was changed to the dispersion liquid 3.
- Example 8 First, the liquid dispersion 4 was applied onto the surface of the metal foil 7 by roll-to-roll coating by the gravure reverse method. Next, the metal foil 7 on which this liquid film was formed was passed through a drying oven at 100° C., 120° C. and 140° C. for a total of 5 minutes, and dried by heating. Then, the dry film was heated at 380° C. for 3 minutes in a far infrared oven under a nitrogen atmosphere. Thereby, the laminated body 8 in which the F layer was formed on the surface of the metal foil layer was manufactured. The thickness of the F layer was 5 ⁇ m.
- the F layer of the laminate 8 and the prepreg 1 were laminated and thermocompression bonded under the conditions of a temperature of 200° C., a pressure of 3 MPa, and a time of 15 minutes.
- all the metal foil layers of the laminated body 8 are removed with an acid solution, and the prepreg 1 is laminated on the contact surface (exposed surface) as it is, and heated at a temperature of 200° C., a pressure of 3 MPa, and a time of 15 minutes. Crimped.
- a composite laminate 8 in which the exposed F layer and the prepreg layer were laminated was obtained.
- Example 9 A composite laminate 9 was produced in the same manner as in Example 8 except that the metal foil 7 was changed to the metal foil 6 and the dispersion liquid 4 was changed to the dispersion liquid 5.
- Example 10 A composite laminate 10 was produced in the same manner as in Example 8 except that the dispersion liquid 4 was changed to the dispersion liquid 5.
- Example 11 comparative example
- a composite laminate 11 was produced in the same manner as in Example 10 except that the metal foil 7 was changed to the metal foil 8 and the thickness of the F layer was 15 ⁇ m.
- Example 12 First, the sheet 1 was laminated on the surface of the metal foil 7 and thermocompression bonded for 3 minutes at 380° C. in an oven under a nitrogen atmosphere. This produced the laminated body in which the F layer was formed on the surface of the metal foil layer. Next, after the F layer side of the laminate was subjected to vacuum plasma treatment, the F layer of the laminate and the prepreg 1 were laminated and thermocompression bonded under the conditions of a temperature of 200° C., a pressure of 3 MPa, and a time of 15 minutes.
- Example 13 A composite laminate 13 was produced in the same manner as in Example 12 except that the sheet 1 was changed to the sheet 2.
- the laminate 1 since the surface of the metal foil was not treated with the silane coupling agent, high peel strength was obtained, and variation in peel strength between samples was small. On the other hand, in the laminate 2, since the surface of the metal foil was treated with the silane coupling agent, not only sufficient peel strength could not be obtained, but also variation in peel strength between samples was large. Further, in the laminate 3, since the F polymer 2 having no oxygen-containing polar group was used, a metal foil whose surface was not treated with a silane coupling agent was used, but the peel strength was low.
- Retention rate (%) (Peeling strength after heating)/(Initial peeling strength) ⁇ 100 The results are summarized in Table 2.
- the laminated body 41 was used to form a sample circuit of a microstrip line.
- the line width of the signal layer was 120 ⁇ m, the line length was 50 mm, and the back surface was a solid ground layer.
- the sample circuit was sandwiched by UTF (Universal Test Fixture), and the transmission loss at 40 GHz was measured using a network analyzer.
- the transmission loss of each of the laminated body 51 and the laminated body 61 was measured in the same manner as the laminated body 41. The results are summarized in Table 3.
- solder resist was dried at 80° C. for 3 minutes, exposed to UV light of 400 mJ/cm 2 , and then immersed in a 1 mass% sodium carbonate aqueous solution for 60 seconds to develop. After that, the solder resist is post-cured at 150° C. for 60 minutes, further exposed to UV light of 1000 mJ/cm 2 to form a solder mask layer, and a composite laminate in which the exposed F layer and the solder mask layer are laminated. I got 14.
- Example 15 A composite laminate 15 was obtained in the same manner as in Example 14 except that the metal foil 8 was used.
- Example 16 A composite laminate 16 was obtained in the same manner as in Example 14 except that the contact surface (exposed surface) of the F layer was treated with a soft etching agent, buffed, and then solder resist was applied.
- the laminate of the present invention and the composite laminate produced by the present invention have excellent electrical properties and adhesiveness, and have a polymer layer firmly fixed to a metal foil layer. Therefore, the antenna component, the printed wiring board, and the power semiconductor It can be used after being processed into insulating layers, aircraft parts, automobile parts, etc.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Microelectronics & Electronic Packaging (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Manufacturing & Machinery (AREA)
- Electrochemistry (AREA)
- Life Sciences & Earth Sciences (AREA)
- Wood Science & Technology (AREA)
- Laminated Bodies (AREA)
Abstract
【課題】ポリマー層と金属箔層との間に均一かつ高い接着性が得られる積層体、及びその製造方法の提供。
【解決手段】本発明の積層体は、金属箔層と、前記金属箔層の表面に直接接触して設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体であって、前記金属箔層が、前記表面にケイ素原子が存在しない金属箔層、又は前記表面を蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔層である。
Description
本発明は、所定の金属箔層の表面に直接接触して設けられた、所定のポリマー層を有する積層体及びその製造方法、複合積層体の製造方法、並びにポリマーフィルムの製造方法に関する。
プリント配線板では、低誘電率化を目的として、銅箔の表面粗さの低減と、低誘電率ポリマーを用いたポリマー層の形成とが行われる。しかし、低誘電率ポリマーは、極性が概して低く、他の材料との接着力が乏しい。また、表面粗さが低減された銅箔は、表面の平滑性が高過ぎるため、ポリマー層のアンカー効果が生じ難く接着性に劣る。したがって、低誘電率ポリマーを含むポリマー層と低粗度化銅箔との強固な接着が困難である。
銅箔とポリマー層との接着力を向上させるために、銅箔の表面は、シランカップリング剤等のケイ素原子を含む表面処理剤で処理される。市販のプリント配線板で使用される銅箔は、その表面がシランカップリング剤で処理さていると言っても過言ではない。
近年、低誘電率ポリマーとしてテトラフルオロエチレン系ポリマー(TFE系ポリマー)が注目されているが、TFE系ポリマーは、特に他の材料との接着性に乏しい。このため、やはり銅箔の表面をシランカップリング剤で処理して、銅箔との接着性を高めている(特許文献1参照)。
近年、低誘電率ポリマーとしてテトラフルオロエチレン系ポリマー(TFE系ポリマー)が注目されているが、TFE系ポリマーは、特に他の材料との接着性に乏しい。このため、やはり銅箔の表面をシランカップリング剤で処理して、銅箔との接着性を高めている(特許文献1参照)。
また、プリント配線板において、配線の微細化が進み、配線同士の離間距離が30μm以下となっているプリント配線板も存在する。このような離間距離になると、銅箔から銅イオンが溶出し、配線同士が短絡する現象(マイグレーション)が生じやすい。そこで、銅の酸化による銅イオンの溶出を防止するため、銅箔とポリマー層(絶縁層)との間にバリア層として、ニッケル、コバルト、亜鉛等の金属層が設けられる場合がある(特許文献2及び3参照)。
ニッケルは、バリア層として優れる反面、その抵抗率が銅に比して高いため、ニッケルを多量で含むプリント配線板は、伝送損失が大きくなる。また、ニッケル自体が高温で変性しやすいため、プリント配線板の製造過程における高温暴露後に、ポリマー層と銅箔との接着性が低下しやすい。
かかる問題を解決するため、銅箔の表面に、コバルトとモリブデンとを含有する酸化防止処理層を設けることが提案されている(特許文献4参照)。
かかる問題を解決するため、銅箔の表面に、コバルトとモリブデンとを含有する酸化防止処理層を設けることが提案されている(特許文献4参照)。
さらに、プリント配線板を製造する際には、TFE系ポリマー層付銅箔の銅箔を回路パターンに加工した後、回路パターンの全体を覆うように、TFE系ポリマー層にプリプレグを接着して積層する場合がある。この場合、TFE系ポリマー層とプリプレグとの接着力が低く、これらの間で層間剥離が起きやすい。そのため、プリプレグを接着する前に、TFE系ポリマー層の表面を表面処理(シランカップリング剤処理、プラズマ処理等)して接着性を高めている(特許文献5及び6参照)。
しかし、本発明者らの検討によれば、TFE系ポリマーは、シランカップリング剤との相互作用にも乏しいため、シランカップリング剤による、TFE系ポリマーと銅箔との接着性の向上効果は限定的であった。また、シランカップリング剤は、その反応性のばらつきや、銅箔の表面への付着量のばらつきが生じやすく、TFE系ポリマーの銅箔との接着性における不安定要素となっている。本発明者らは、所定のTFE系ポリマー及び金属箔を使用すれば、シランカップリング剤による不安定要素の排除が可能であることを知見した。
また、本発明者らの検討によれば、低誘電率ポリマーとしてTFE系ポリマーを用いた場合、上述したコバルトやモリブデンを含む層とTFE系ポリマーとは初期接着力が著しく低く、高温暴露後の接着力も未だ充分ではなかった。そこで、本発明者らは、初期接着力を改善すべく鋭意検討した結果、ニッケルが所定の微量範囲で存在する表面を有する金属箔を使用し、かかる金属箔の表面に所定のTFE系ポリマーを含むポリマー層を設ければ、初期接着力と高温暴露後の接着力とのいずれにも優れ、電気特性にも優れる積層体が得られることを知見した。
さらに、本発明者らは、所定の表面性状を有する金属箔を使用すれば、プリプレグに対して高い接着力を発揮するTFE系ポリマーを含むポリマー層が得られることを知見し、本発明を完成した。
すなわち、本発明は、ポリマー層と金属箔層との間に均一かつ高い接着性が得られる積層体、及びその製造方法の提供を目的とする。
また、本発明は、ポリマー層と金属箔層との間に、高い初期接着力があり高温熱履歴を経た後でも高い接着力が維持される、電気特性に優れた積層体、及びその製造方法の提供を目的とする。
さらに、本発明は、表面処理を省略しても、プリプレグ等に対する高い接着力を発揮するポリマーフィルムの製造方法、及びポリマー層とプリプレグ層との間での剥離が生じ難い複合積層体の製造方法の提供を目的とする。
また、本発明は、ポリマー層と金属箔層との間に、高い初期接着力があり高温熱履歴を経た後でも高い接着力が維持される、電気特性に優れた積層体、及びその製造方法の提供を目的とする。
さらに、本発明は、表面処理を省略しても、プリプレグ等に対する高い接着力を発揮するポリマーフィルムの製造方法、及びポリマー層とプリプレグ層との間での剥離が生じ難い複合積層体の製造方法の提供を目的とする。
本発明は、下記の態様を有する。
<1> 金属箔層と、前記金属箔層の表面に直接接触して設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体であって、前記金属箔層が、前記表面にケイ素原子が存在しない金属箔層、又は前記表面を蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔層である、積層体。
<2> 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備える、上記<1>の積層体。
<3> 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備え、前記金属粒子は、銅、ニッケル、リン、タングステン、ヒ素、モリブデン、クロム、コバルト、亜鉛又はこれらの1種以上を含む合金で形成されている、上記<1>又は<2>の積層体。
<4> 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備え、前記金属粒子は、針状をなす金属粒子を含む、上記<1>~<3>のいずれかの積層体。
<5> 前記金属箔層の前記表面の十点平均粗さが、0.1μm以上である、上記<1>~<4>のいずれかの積層体。
<6> 前記テトラフルオロエチレン系ポリマーが、ペルフルオロ(アルキルビニルエーテル)に基づく単位に基づく単位を含むテトラフルオロエチレン系ポリマー、又は、数平均分子量が20万以下であるポリテトラフルオロエチレンである、上記<1>~<5>のいずれかの積層体。
<7> 前記テトラフルオロエチレン系ポリマーが、ペルフルオロ(アルキルビニルエーテル)に基づく単位を含み、酸素含有極性基を有するテトラフルオロエチレン系ポリマー、又は、ペルフルオロ(アルキルビニルエーテル)に基づく単位を全単位に対して2.0~5.0モル%含み、酸素含有極性基を有さないテトラフルオロエチレン系ポリマーである、上記<1>~<6>のいずれかの積層体。
<8> 前記ポリマー層の前記金属箔層に対する剥離強度が、10N/cm以上である、上記<1>~<7>のいずれかの積層体。
<9> 金属箔の表面をシランカップリング剤で処理することなく、前記金属箔の前記表面に、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層を直接接触して形成し、前記金属箔で構成される金属箔層の表面に直接接触して設けられた前記ポリマー層を有する積層体を得る、積層体の製造方法。
<10> 蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔の表面に、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層を直接接触して形成し、前記金属箔で構成される金属箔層の表面に直接接触して設けられた前記ポリマー層を有する積層体を得る、積層体の製造方法。
<11> 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層の少なくとも一部を除去し、露出した前記ポリマー層とプリプレグとを接着させ、少なくとも前記ポリマー層とプリプレグ層とが積層された複合積層体を得る、複合積層体の製造方法。
<12> 前記露出した前記ポリマー層の表面を親水化処理することなく、前記プリプレグと接着させる、上記<11>の製造方法。
<13> 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層の少なくとも一部を除去し、露出した前記ポリマー層にソルダーレジストを塗布し、硬化させてソルダーマスク層を形成し、少なくとも前記ポリマー層とソルダーマスク層とが積層された複合積層体を得る、複合積層体の製造方法。
<14> 前記露出した前記ポリマー層の表面を酸溶液で処理し、そのまま直接、ソルダーレジストを塗布し、硬化させてソルダーマスク層を形成する、上記<13>の製造方法。
<15> 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層を除去して、残存する前記ポリマー層をポリマーフィルムとする、ポリマーフィルムの製造方法。
<1> 金属箔層と、前記金属箔層の表面に直接接触して設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体であって、前記金属箔層が、前記表面にケイ素原子が存在しない金属箔層、又は前記表面を蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔層である、積層体。
<2> 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備える、上記<1>の積層体。
<3> 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備え、前記金属粒子は、銅、ニッケル、リン、タングステン、ヒ素、モリブデン、クロム、コバルト、亜鉛又はこれらの1種以上を含む合金で形成されている、上記<1>又は<2>の積層体。
<4> 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備え、前記金属粒子は、針状をなす金属粒子を含む、上記<1>~<3>のいずれかの積層体。
<5> 前記金属箔層の前記表面の十点平均粗さが、0.1μm以上である、上記<1>~<4>のいずれかの積層体。
<6> 前記テトラフルオロエチレン系ポリマーが、ペルフルオロ(アルキルビニルエーテル)に基づく単位に基づく単位を含むテトラフルオロエチレン系ポリマー、又は、数平均分子量が20万以下であるポリテトラフルオロエチレンである、上記<1>~<5>のいずれかの積層体。
<7> 前記テトラフルオロエチレン系ポリマーが、ペルフルオロ(アルキルビニルエーテル)に基づく単位を含み、酸素含有極性基を有するテトラフルオロエチレン系ポリマー、又は、ペルフルオロ(アルキルビニルエーテル)に基づく単位を全単位に対して2.0~5.0モル%含み、酸素含有極性基を有さないテトラフルオロエチレン系ポリマーである、上記<1>~<6>のいずれかの積層体。
<8> 前記ポリマー層の前記金属箔層に対する剥離強度が、10N/cm以上である、上記<1>~<7>のいずれかの積層体。
<9> 金属箔の表面をシランカップリング剤で処理することなく、前記金属箔の前記表面に、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層を直接接触して形成し、前記金属箔で構成される金属箔層の表面に直接接触して設けられた前記ポリマー層を有する積層体を得る、積層体の製造方法。
<10> 蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔の表面に、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層を直接接触して形成し、前記金属箔で構成される金属箔層の表面に直接接触して設けられた前記ポリマー層を有する積層体を得る、積層体の製造方法。
<11> 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層の少なくとも一部を除去し、露出した前記ポリマー層とプリプレグとを接着させ、少なくとも前記ポリマー層とプリプレグ層とが積層された複合積層体を得る、複合積層体の製造方法。
<12> 前記露出した前記ポリマー層の表面を親水化処理することなく、前記プリプレグと接着させる、上記<11>の製造方法。
<13> 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層の少なくとも一部を除去し、露出した前記ポリマー層にソルダーレジストを塗布し、硬化させてソルダーマスク層を形成し、少なくとも前記ポリマー層とソルダーマスク層とが積層された複合積層体を得る、複合積層体の製造方法。
<14> 前記露出した前記ポリマー層の表面を酸溶液で処理し、そのまま直接、ソルダーレジストを塗布し、硬化させてソルダーマスク層を形成する、上記<13>の製造方法。
<15> 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層を除去して、残存する前記ポリマー層をポリマーフィルムとする、ポリマーフィルムの製造方法。
本発明によれば、ポリマー層と金属箔との間に均一かつ高い接着性が得られる積層体、及びその製造方法が提供される。
また、本発明によれば、ポリマー層と金属箔との間に、高い初期接着力があり高温熱履歴を経た後でも高い接着力が維持される、電気特性に優れた積層体、及びその製造方法が提供される。
さらに、本発明によれば、プリプレグ等に対する高い接着力を発揮するポリマーフィルム、及びポリマー層とプリプレグ層との間での剥離が生じ難い複合積層体が提供される。
また、本発明によれば、ポリマー層と金属箔との間に、高い初期接着力があり高温熱履歴を経た後でも高い接着力が維持される、電気特性に優れた積層体、及びその製造方法が提供される。
さらに、本発明によれば、プリプレグ等に対する高い接着力を発揮するポリマーフィルム、及びポリマー層とプリプレグ層との間での剥離が生じ難い複合積層体が提供される。
以下の用語は、以下の意味を有する。
「パウダーのD50」は、レーザー回折・散乱法によってパウダーの粒度分布を測定し、パウダーを構成する粒子(以下、「パウダー粒子」とも記す。)の集団の全体積を100%として累積カーブを求め、その累積カーブ上で累積体積が50%となる点の粒子径(体積基準累積50%径)である。
「パウダーのD90」は、レーザー回折・散乱法によってパウダーの粒度分布を測定し、パウダー粒子の集団の全体積を100%として累積カーブを求め、その累積カーブ上で累積体積が90%となる点の粒子径(体積基準累積90%径)である。
つまり、パウダーのD50及びD90は、それぞれ、パウダー粒子の体積基準累積50%径及び体積基準累積90%径である。
「ポリマーの溶融粘度」は、ASTM D 1238に準拠し、フローテスター及び2Φ-8Lのダイを用い、予め測定温度にて5分間加熱しておいたポリマーの試料(2g)を0.7MPaの荷重にて測定温度に保持して測定した値である。
「ポリマーの溶融温度(融点)」は、示差走査熱量測定(DSC)法で測定したポリマーの融解ピークの最大値に対応する温度である。
「粘度」は、B型粘度計を用いて、室温下(25℃)で回転数が30rpmの条件下で測定される値である。測定を3回繰り返し、3回分の測定値の平均値とする。
「十点平均粗さ(Rzjis)」は、JIS B 0601:2013の附属書JAで規定される値である。
「剥離強度」とは、矩形状(長さ100mm、幅10mm)に切り出した積層体の長さ方向の一端から50mmの位置を固定し、引張り速度50mm/分、長さ方向の片端から積層体に対して90°で、金属箔とポリマー層とを剥離させた際にかかる最大荷重(N/cm)である。
ポリマーにおける「単位」は、重合反応によってモノマーから直接形成された原子団であってもよく、重合反応によって得られたポリマーを所定の方法で処理して、構造の一部が変換された原子団であってもよい。ポリマーに含まれる、モノマーAに基づく単位を、単に「モノマーA単位」とも記す。
「パウダーのD50」は、レーザー回折・散乱法によってパウダーの粒度分布を測定し、パウダーを構成する粒子(以下、「パウダー粒子」とも記す。)の集団の全体積を100%として累積カーブを求め、その累積カーブ上で累積体積が50%となる点の粒子径(体積基準累積50%径)である。
「パウダーのD90」は、レーザー回折・散乱法によってパウダーの粒度分布を測定し、パウダー粒子の集団の全体積を100%として累積カーブを求め、その累積カーブ上で累積体積が90%となる点の粒子径(体積基準累積90%径)である。
つまり、パウダーのD50及びD90は、それぞれ、パウダー粒子の体積基準累積50%径及び体積基準累積90%径である。
「ポリマーの溶融粘度」は、ASTM D 1238に準拠し、フローテスター及び2Φ-8Lのダイを用い、予め測定温度にて5分間加熱しておいたポリマーの試料(2g)を0.7MPaの荷重にて測定温度に保持して測定した値である。
「ポリマーの溶融温度(融点)」は、示差走査熱量測定(DSC)法で測定したポリマーの融解ピークの最大値に対応する温度である。
「粘度」は、B型粘度計を用いて、室温下(25℃)で回転数が30rpmの条件下で測定される値である。測定を3回繰り返し、3回分の測定値の平均値とする。
「十点平均粗さ(Rzjis)」は、JIS B 0601:2013の附属書JAで規定される値である。
「剥離強度」とは、矩形状(長さ100mm、幅10mm)に切り出した積層体の長さ方向の一端から50mmの位置を固定し、引張り速度50mm/分、長さ方向の片端から積層体に対して90°で、金属箔とポリマー層とを剥離させた際にかかる最大荷重(N/cm)である。
ポリマーにおける「単位」は、重合反応によってモノマーから直接形成された原子団であってもよく、重合反応によって得られたポリマーを所定の方法で処理して、構造の一部が変換された原子団であってもよい。ポリマーに含まれる、モノマーAに基づく単位を、単に「モノマーA単位」とも記す。
本発明の積層体(本積層体)は、金属箔層と、金属箔層の表面に直接接触して設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマー(以下、「Fポリマー」とも記す。)を含むポリマー層(以下、「F層」とも記す。)とを有する。
本積層体における金属箔層は、上記表面にケイ素原子が存在しない金属箔層(以下、「金属箔層1」とも記す。)、又は上記表面を蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔層(以下、「金属箔層2」とも記す。)である。
以下、金属箔層1を有する本積層体を本積層体1とも、金属箔層2を有する本積層体を本積層体2とも記す。
本積層体における金属箔層は、上記表面にケイ素原子が存在しない金属箔層(以下、「金属箔層1」とも記す。)、又は上記表面を蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔層(以下、「金属箔層2」とも記す。)である。
以下、金属箔層1を有する本積層体を本積層体1とも、金属箔層2を有する本積層体を本積層体2とも記す。
本積層体1は、金属箔層1と、この金属箔層1の表面に直接接触して設けられたF層とを有する。なお、F層は、金属箔層1の一方の表面にのみ設けられても、双方の表面に設けられてもよい。
本積層体1では、金属箔層1の表面(F層側の表面)にケイ素原子が存在しない。これは、金属箔層1の表面がシランカップリング剤で処理されていないことを意味している。すなわち、本積層体1の製造方法は、金属箔層1の表面をシランカップリング剤で処理することなく、この表面にF層を直接接触して形成する方法である。
なお、金属箔層1の表面にケイ素原子が存在するか否かは、金属箔層1の表面を蛍光X線分析(XRF)法により分析して確認できる。この分析により、ケイ素原子の検出量が検出限界以下であればよい。
本積層体1では、金属箔層1の表面(F層側の表面)にケイ素原子が存在しない。これは、金属箔層1の表面がシランカップリング剤で処理されていないことを意味している。すなわち、本積層体1の製造方法は、金属箔層1の表面をシランカップリング剤で処理することなく、この表面にF層を直接接触して形成する方法である。
なお、金属箔層1の表面にケイ素原子が存在するか否かは、金属箔層1の表面を蛍光X線分析(XRF)法により分析して確認できる。この分析により、ケイ素原子の検出量が検出限界以下であればよい。
金属箔層1を構成する金属箔は、その表面に酸化により生成された酸化物(水酸化物等)が存在していると考えられる。一方、所定の溶融粘度を有するFポリマーは、金属箔の表面に存在する酸化物及び/又は金属原子と相互作用しやすい、特にFポリマーが酸素含有極性基を含有すれば、この酸素含有極性基が金属箔の表面に存在する酸化物及び/又は金属原子と強く相互作用すると考えられる。その結果、本積層体1では、Fポリマーを含むF層が、金属箔との高い接着性を発現したと推察される。
なお、シランカップリング剤による処理は、シランカップリング剤を含む溶液の金属箔の表面での濡れ広がりを利用して行われる。このため、初期段階でシランカップリング剤が結合した部分に溶液が集まりやすくなり、シランカップリング剤が結合した部分と結合していない部分とが島状に散在し、金属箔の表面に存在するシランカップリング剤の量にばらつきが生じると考えられる。また、その程度は、金属箔の表面性状に大きく影響を受ける。したがって、かかる状態の金属箔の表面にF層を形成すると、F層と金属箔との間に均一な接着性が発現しにくい。これに対して、本積層体1では、金属箔の表面をシランカップリング剤で処理しないため、上記不都合が発生するのを防止でき、F層と金属箔(金属箔層1)との間に均一な接着性が得られたと推察される。
なお、シランカップリング剤による処理は、シランカップリング剤を含む溶液の金属箔の表面での濡れ広がりを利用して行われる。このため、初期段階でシランカップリング剤が結合した部分に溶液が集まりやすくなり、シランカップリング剤が結合した部分と結合していない部分とが島状に散在し、金属箔の表面に存在するシランカップリング剤の量にばらつきが生じると考えられる。また、その程度は、金属箔の表面性状に大きく影響を受ける。したがって、かかる状態の金属箔の表面にF層を形成すると、F層と金属箔との間に均一な接着性が発現しにくい。これに対して、本積層体1では、金属箔の表面をシランカップリング剤で処理しないため、上記不都合が発生するのを防止でき、F層と金属箔(金属箔層1)との間に均一な接着性が得られたと推察される。
本積層体2は、金属箔層2と、この金属箔層2の表面に直接接触して設けられたF層とを有する。なお、F層は、金属箔層2の一方の表面にのみ設けられても、双方の表面に設けられてもよい。
本積層体2では、金属箔層2の表面(F層側の表面)に所定量(微量)のニッケル原子が存在する。本積層体2の製造方法は、所定量でニッケル原子が存在する金属箔の表面にF層を直接接触して形成する方法である。
なお、金属箔の表面に存在するニッケル原子の割合は、金属箔の表面を蛍光X線分析(XRF)法により分析して測定できる。
本積層体2では、金属箔層2の表面(F層側の表面)に所定量(微量)のニッケル原子が存在する。本積層体2の製造方法は、所定量でニッケル原子が存在する金属箔の表面にF層を直接接触して形成する方法である。
なお、金属箔の表面に存在するニッケル原子の割合は、金属箔の表面を蛍光X線分析(XRF)法により分析して測定できる。
金属箔層2を構成する金属箔は、その表面に酸化により生成されたニッケルの酸化物(水酸化物等)が存在していると考えられる。一方、所定の溶融粘度を有するFポリマーは、金属箔の表面に存在する、この酸化物やニッケル原子と強く相互作用しやすい、特にFポリマーが酸素含有極性基を含有すれば、この酸素含有極性基がこの酸化物やニッケル原子と強く相互作用すると考えられる。その結果、本積層体2では、Fポリマーを含むF層が、金属箔(金属箔層2)との高い初期接着性を発現したと推察される。
また、ニッケル原子の存在により、Fポリマーによる金属箔の表面の劣化(腐食)を防止する効果が発揮されると考えられる。このため、本積層体2は、高温での熱履歴を経た後も、F層と金属箔(金属箔層2)との間に高い接着力が維持されたと推察される。
また、ニッケル原子の存在により、Fポリマーによる金属箔の表面の劣化(腐食)を防止する効果が発揮されると考えられる。このため、本積層体2は、高温での熱履歴を経た後も、F層と金属箔(金属箔層2)との間に高い接着力が維持されたと推察される。
本発明におけるFポリマーは、テトラフルオロエチレン(TFE)に基づく単位(TFE単位)を含むポリマーであり、熱溶融加工性ポリマーであるのが好ましい。
Fポリマーの380℃における溶融粘度は、1×10²~1×10⁶Pa・sであり、1×10³~1×10⁶Pa・sが好ましい。
Fポリマーの溶融温度は、140~320℃が好ましく、200~320℃がより好ましく、260~320℃がさらに好ましい。この場合、F層の金属箔(金属箔層1及び2)に対する接着性を更に向上させやすい。
Fポリマーの380℃における溶融粘度は、1×10²~1×10⁶Pa・sであり、1×10³~1×10⁶Pa・sが好ましい。
Fポリマーの溶融温度は、140~320℃が好ましく、200~320℃がより好ましく、260~320℃がさらに好ましい。この場合、F層の金属箔(金属箔層1及び2)に対する接着性を更に向上させやすい。
Fポリマーは、酸素含有極性基を有するのが好ましい。
Fポリマーが有する酸素含有極性基は、酸素含有極性基を有するモノマーに基づく単位に含まれていてもよく、ポリマー主鎖末端部に含まれていてもよく、表面処理(放射線処理、電子線処理、コロナ処理、プラズマ処理等)によりポリマー中に含まれていてもよく、最前者が好ましい。また、Fポリマーが有する酸素含有極性基は、酸素含有極性基を形成し得る基を有するポリマーを変性して調製された基であってもよい。ポリマー末端基に含まれる酸素含有極性基は、そのポリマーの重合に際して使用する成分(重合開始剤、連鎖移動剤等)を調整して得られる。
酸素含有極性基は、酸素原子を含有する極性の原子団である。ただし、本発明における酸素含有極性基には、エステル結合自体とエーテル結合自体とは含まれず、これらの結合を特性基として含む原子団は含まれる。
Fポリマーが有する酸素含有極性基は、酸素含有極性基を有するモノマーに基づく単位に含まれていてもよく、ポリマー主鎖末端部に含まれていてもよく、表面処理(放射線処理、電子線処理、コロナ処理、プラズマ処理等)によりポリマー中に含まれていてもよく、最前者が好ましい。また、Fポリマーが有する酸素含有極性基は、酸素含有極性基を形成し得る基を有するポリマーを変性して調製された基であってもよい。ポリマー末端基に含まれる酸素含有極性基は、そのポリマーの重合に際して使用する成分(重合開始剤、連鎖移動剤等)を調整して得られる。
酸素含有極性基は、酸素原子を含有する極性の原子団である。ただし、本発明における酸素含有極性基には、エステル結合自体とエーテル結合自体とは含まれず、これらの結合を特性基として含む原子団は含まれる。
酸素含有極性基は、水酸基含有基、カルボニル基含有基、アセタール基及びオキシシクロアルカン基からなる群から選ばれる少なくとも1種の基が好ましく、水酸基含有基又はカルボニル基含有基がより好ましく、-CF2CH2OH、-C(CF3)2OH、1,2-グリコール基(-CH(OH)CH2OH)、-CF2C(O)OH、>CFC(O)OH、カルボキシアミド基(-C(O)NH2等)、酸無水物残基(-C(O)OC(O)-)、イミド残基(-C(O)NHC(O)-等)、ジカルボン酸残基(-CH(C(O)OH)CH2C(O)OH等)又はカーボネート基(-OC(O)O-)がさらに好ましい。
また、F層の金属箔に対する接着性を損ないにくい観点から、酸素含有極性基は、極性基であり環状基であるかその開環基である、環状酸無水物残基、環状イミド残基、環状カーボネート基、環状アセタール基、1,2-ジカルボン酸残基又は1,2-グリコール基が特に好ましく、環状酸無水物残基が最も好ましい。
オキシシクロアルカン基は、エポキシ基又はオキセタニル基が好ましい。
また、F層の金属箔に対する接着性を損ないにくい観点から、酸素含有極性基は、極性基であり環状基であるかその開環基である、環状酸無水物残基、環状イミド残基、環状カーボネート基、環状アセタール基、1,2-ジカルボン酸残基又は1,2-グリコール基が特に好ましく、環状酸無水物残基が最も好ましい。
オキシシクロアルカン基は、エポキシ基又はオキセタニル基が好ましい。
Fポリマーは、TFE単位と、ヘキサフルオロプロピレン(HFP)、ペルフルオロ(アルキルビニルエーテル)(PAVE)又はフルオロアルキルエチレン(FAE)に基づく単位(以下、「PAE単位」とも記す。)と、酸素含有極性基を有するモノマーに基づく単位(以下、「極性単位」とも記す。)とを含むポリマーが好ましい。
TFE単位の割合は、Fポリマーを構成する全単位のうち、50~99モル%が好ましく、90~99モル%が特に好ましい。
PAE単位は、PAVEに基づく単位又はHFPに基づく単位が好ましく、PAVEに基づく単位が特に好ましい。PAE単位は、2種類以上であってもよい。
TFE単位の割合は、Fポリマーを構成する全単位のうち、50~99モル%が好ましく、90~99モル%が特に好ましい。
PAE単位は、PAVEに基づく単位又はHFPに基づく単位が好ましく、PAVEに基づく単位が特に好ましい。PAE単位は、2種類以上であってもよい。
PAVEとしては、CF2=CFOCF3(PMVE)、CF2=CFOCF2CF3、CF2=CFOCF2CF2CF3(PPVE)、CF2=CFOCF2CF2CF2CF3、CF2=CFO(CF2)8Fが挙げられ、PMVE又はPPVEが好ましい。
FAEとしては、CH2=CH(CF2)2F(PFEE)、CH2=CH(CF2)3F、CH2=CH(CF2)4F(PFBE)、CH2=CF(CF2)3H、CH2=CF(CF2)4Hが挙げられ、PFEE又はPFBEが好ましい。
PAE単位の割合は、Fポリマーを構成する全単位のうち、0.5~9.97モル%が好ましく、0.5~9.97モル%がより好ましい。
FAEとしては、CH2=CH(CF2)2F(PFEE)、CH2=CH(CF2)3F、CH2=CH(CF2)4F(PFBE)、CH2=CF(CF2)3H、CH2=CF(CF2)4Hが挙げられ、PFEE又はPFBEが好ましい。
PAE単位の割合は、Fポリマーを構成する全単位のうち、0.5~9.97モル%が好ましく、0.5~9.97モル%がより好ましい。
極性単位は、酸無水物残基、カーボネート基、環状アセタール基、1,2-ジカルボン酸残基、1,2-ジオール残基、又は1,3-ジオール残基を有するモノマーに基づく単位が好ましく、環状酸無水物残基、又は環状カーボネート基を有するモノマー単位がより好ましく、環状酸無水物残基を有するモノマー単位がより好ましい。極性単位は、1種類であってもよく、2種類以上であってもよい。
環状酸無水物残基を有するモノマーは、無水イタコン酸、無水シトラコン酸、5-ノルボルネン-2,3-ジカルボン酸無水物(別称:無水ハイミック酸;以下、「NAH」とも記す。)又は無水マレイン酸が好ましく、NAHがより好ましい。
極性単位の割合は、Fポリマーを構成する全単位のうち、0.01~3モル%が好ましい。
環状酸無水物残基を有するモノマーは、無水イタコン酸、無水シトラコン酸、5-ノルボルネン-2,3-ジカルボン酸無水物(別称:無水ハイミック酸;以下、「NAH」とも記す。)又は無水マレイン酸が好ましく、NAHがより好ましい。
極性単位の割合は、Fポリマーを構成する全単位のうち、0.01~3モル%が好ましい。
また、この場合のFポリマーは、TFE単位、PAE単位及び極性単位以外の単位(以下、「他の単位」とも記す。)を、さらに含んでいてもよい。他の単位は、1種類であってもよく、2種類以上であってもよい。
他の単位を形成するモノマーとしては、エチレン、プロピレン、塩化ビニル、塩化ビニリデン、フッ化ビニル、フッ化ビニリデン(VDF)、クロロトリフルオロエチレン(CTFE)が挙げられる。他の単位は、エチレン、VDF又はCTFEが好ましく、エチレンがより好ましい。
Fポリマーにおける他の単位の割合は、Fポリマーを構成する全単位のうち、0~50モル%が好ましく、0~40モル%がより好ましい。
他の単位を形成するモノマーとしては、エチレン、プロピレン、塩化ビニル、塩化ビニリデン、フッ化ビニル、フッ化ビニリデン(VDF)、クロロトリフルオロエチレン(CTFE)が挙げられる。他の単位は、エチレン、VDF又はCTFEが好ましく、エチレンがより好ましい。
Fポリマーにおける他の単位の割合は、Fポリマーを構成する全単位のうち、0~50モル%が好ましく、0~40モル%がより好ましい。
Fポリマーの好適な態様としては、PAVEに基づく単位(PAVE単位)を含むFポリマー、又は、数平均分子量が20万以下であるPTFEが挙げられる。
なお、上記PTFEの数平均分子量は、下式(1)に基づいて算出される値である。
Mn = 2.1×10¹⁰×ΔHc-5.16 ・・・ (1)
式(1)中、Mnは、上記PTFEの数平均分子量を、ΔHcは、示差走査熱量分析法により測定される上記PTFEの結晶化熱量(cal/g)を、それぞれ示す。
上記PTFEのMnは、10以下が好ましく、5万以下がより好ましい。上記PTFEのMnは、1万以上が好ましい。
なお、上記PTFEの数平均分子量は、下式(1)に基づいて算出される値である。
Mn = 2.1×10¹⁰×ΔHc-5.16 ・・・ (1)
式(1)中、Mnは、上記PTFEの数平均分子量を、ΔHcは、示差走査熱量分析法により測定される上記PTFEの結晶化熱量(cal/g)を、それぞれ示す。
上記PTFEのMnは、10以下が好ましく、5万以下がより好ましい。上記PTFEのMnは、1万以上が好ましい。
Fポリマーのより好適な態様としては、PAVEに基づく単位を含み、酸素含有極性基を有するFポリマー、又は、PAVEに基づく単位を全単位に対して2.0~5.0モル%含み、酸素含有極性基を有さないFポリマーが挙げられる。
この態様のFポリマーは、F層において微小球晶を形成しやすく、他の成分との密着性が高まりやすい。
この態様のFポリマーは、F層において微小球晶を形成しやすく、他の成分との密着性が高まりやすい。
前者のポリマーは、全単位に対して、TFE単位を90~99モル%、PAVE単位を0.5~9.97モル%及び極性単位を0.01~3モル%、それぞれ含有するのが好ましい。
後者のポリマーにおけるPAVE単位の含有量は、全単位に対して、2.1モル%以上が好ましく、2.2モル%以上がより好ましい。
後者のポリマーは、TFE単位及びPAVE単位のみからなり、全単位に対して、TFE単位を95.0~98.0モル%、PAVE単位を2.0~5.0モル%含有するのが好ましい。
後者のポリマーにおけるPAVE単位の含有量は、全単位に対して、2.1モル%以上が好ましく、2.2モル%以上がより好ましい。
後者のポリマーは、TFE単位及びPAVE単位のみからなり、全単位に対して、TFE単位を95.0~98.0モル%、PAVE単位を2.0~5.0モル%含有するのが好ましい。
なお、後者のポリマーが酸素含有極性基を有さないとは、ポリマー主鎖を構成する炭素原子数の1×10⁶個あたりに対して、ポリマーが有する酸素含有極性基が、500個未満であることを意味する。上記酸素含有極性基数は、100個以下が好ましく、50個以下がより好ましい。上記酸素含有極性基数の下限は、通常、0個である。
後者のポリマーは、ポリマー鎖の末端基として酸素含有極性基を生じない、重合開始剤や連鎖移動剤等を使用して製造してもよく、酸素含有極性基を有するFポリマー(重合開始剤に由来する酸素含有極性基をポリマーの主鎖の末端基に有するFポリマー等)をフッ素化処理して製造してもよい。フッ素化処理の方法としては、フッ素ガスを使用する方法(特開2019-194314号公報等を参照)が挙げられる。
後者のポリマーは、ポリマー鎖の末端基として酸素含有極性基を生じない、重合開始剤や連鎖移動剤等を使用して製造してもよく、酸素含有極性基を有するFポリマー(重合開始剤に由来する酸素含有極性基をポリマーの主鎖の末端基に有するFポリマー等)をフッ素化処理して製造してもよい。フッ素化処理の方法としては、フッ素ガスを使用する方法(特開2019-194314号公報等を参照)が挙げられる。
金属箔層1及び2とすべき金属箔を構成する金属としては、銅、鉄、ニッケル、アルミニウム、亜鉛、これらの合金(銅合金、ステンレス鋼、ニッケル合金(42合金も含む。)、アルミニウム合金等)が挙げられる。
金属箔としては、銅箔が好ましく、表裏の区別のない圧延銅箔、表裏の区別のある電解銅箔等の銅箔がより好ましく、圧延銅箔がさらに好ましい。圧延銅箔は、表面粗さが小さいため、積層体をプリント配線板に加工した場合でも、伝送損失を低減できる。また、圧延銅箔は、炭化水素系有機溶剤に浸漬し圧延油を除去してから使用するのが好ましい。
F層を形成する面は、圧延銅箔においてはいずれの面でもよく、電解銅箔においても析出面又は光沢面のいずれの面でもよい。
なお、金属箔は、中間層を介してキャリア上に積層されたキャリア付き金属箔であってもよい。
金属箔としては、銅箔が好ましく、表裏の区別のない圧延銅箔、表裏の区別のある電解銅箔等の銅箔がより好ましく、圧延銅箔がさらに好ましい。圧延銅箔は、表面粗さが小さいため、積層体をプリント配線板に加工した場合でも、伝送損失を低減できる。また、圧延銅箔は、炭化水素系有機溶剤に浸漬し圧延油を除去してから使用するのが好ましい。
F層を形成する面は、圧延銅箔においてはいずれの面でもよく、電解銅箔においても析出面又は光沢面のいずれの面でもよい。
なお、金属箔は、中間層を介してキャリア上に積層されたキャリア付き金属箔であってもよい。
また、金属箔は、上記金属で構成された基材層(例えば、銅箔)と、金属粒子(粗化粒子)で構成された粗化処理層とを有する積層構造であってもよい。この場合、粗化処理層の表面が金属箔の表面を構成する。上記粗化処理層としては、ニッケルを含有する金属粒子(粗化粒子)で構成された粗化処理層が挙げられる。
金属粒子は、銅、ニッケル、リン、タングステン、ヒ素、モリブデン、クロム、コバルト、亜鉛又はこれらの1種以上を含む合金で形成されるのが好ましく、銅、ニッケル、コバルト又はこれらの1種以上を含む合金で形成されるのがより好ましい。
金属粒子は、ニッケル単独、又はニッケルと、銅、リン、タングステン、ヒ素、モリブデン、クロム、コバルト及び亜鉛の少なくとも1種との合金で形成されるのがさらに好ましく、ニッケルと、銅及びコバルトの少なくとも1種を含む合金で形成されるのが最も好ましい。かかる金属粒子は、基材層を構成する金属(特に、銅)との密着性に優れる。
金属粒子は、銅、ニッケル、リン、タングステン、ヒ素、モリブデン、クロム、コバルト、亜鉛又はこれらの1種以上を含む合金で形成されるのが好ましく、銅、ニッケル、コバルト又はこれらの1種以上を含む合金で形成されるのがより好ましい。
金属粒子は、ニッケル単独、又はニッケルと、銅、リン、タングステン、ヒ素、モリブデン、クロム、コバルト及び亜鉛の少なくとも1種との合金で形成されるのがさらに好ましく、ニッケルと、銅及びコバルトの少なくとも1種を含む合金で形成されるのが最も好ましい。かかる金属粒子は、基材層を構成する金属(特に、銅)との密着性に優れる。
また、ニッケルを含む粗化処理層は、積層体をプリント配線板に加工する際に、金属箔(金属箔層1及び2)から細幅かつ短い離間距離(例えば、30μm以下)の配線を形成しても、配線同士の間でマイグレーションが発生するのを好適に防止できる。
さらに、ニッケルを含む金属粒子は、針状をなす金属粒子を含むように、基材層上に析出させやすい。針状をなす金属粒子を含む粗化処理層であれば、その表面に対するF層のアンカー効果がより向上し、F層の金属箔に対する接着性を充分に高められる。
さらに、ニッケルを含む金属粒子は、針状をなす金属粒子を含むように、基材層上に析出させやすい。針状をなす金属粒子を含む粗化処理層であれば、その表面に対するF層のアンカー効果がより向上し、F層の金属箔に対する接着性を充分に高められる。
金属箔(金属箔層2)の表面に存在するニッケル原子の割合は、0.03~0.25質量%であり、0.04~0.2質量%が好ましく、0.05~0.15質量%がより好ましい。上記範囲でニッケル原子が存在すれば、Fポリマーによる金属箔の表面の劣化(腐食)を防止する効果がより効果的に発揮されるとともに、ニッケル原子に変性が生じた場合でも、その影響が少ない。したがって、F層の金属箔(金属箔層2)の表面に対する接着性の低下が生じにくい。また、抵抗率が高いニッケル原子の割合が多過ぎないため、積層体をプリント配線板に加工した場合でも、伝送損失の低減を防止できる。
また、かかる積層構成の金属箔においては、粗化処理層の表面に、金属粒子の形状を反映した凹凸が形成される。このため、F層の金属箔(金属箔層1及び2)の表面に対するアンカー効果が好適に発揮され、結果として、F層の金属箔(金属箔層1及び2)に対する接着性(密着性)が向上する。この場合、金属粒子の平均粒径は、0.1~0.25μmが好ましい。
F層の金属箔(金属箔層1及び2)に対する接着性をより高める観点から、金属箔の表面(F層側の表面)の十点平均粗さは、0.1~1.5μmが好ましく、0.3~1.3μmがより好ましい。また、上記範囲の十点平均粗さであれば、金属箔の表面の凹凸の程度が大き過ぎないため、積層体をプリント配線板に加工した場合でも、伝送損失の増大を抑制できる。
F層の金属箔(金属箔層1及び2)に対する接着性をより高める観点から、金属箔の表面(F層側の表面)の十点平均粗さは、0.1~1.5μmが好ましく、0.3~1.3μmがより好ましい。また、上記範囲の十点平均粗さであれば、金属箔の表面の凹凸の程度が大き過ぎないため、積層体をプリント配線板に加工した場合でも、伝送損失の増大を抑制できる。
粗化処理層の表面の十点平均粗さは、金属粒子のサイズ、金属粒子の数等の設定により調整できる。
粗化処理層は、基材層を陰極とした電気めっき法により、金属粒子を基材層上に析出(電着)して形成されるのが好ましい。この場合、金属粒子のサイズ、金属粒子の数等の電着量は、主に電流密度及び電着時間の調整によって制御できる。
電気めっきには、以下に示すめっき条件(1)又はめっき条件(2)が好適に用いられる。
粗化処理層は、基材層を陰極とした電気めっき法により、金属粒子を基材層上に析出(電着)して形成されるのが好ましい。この場合、金属粒子のサイズ、金属粒子の数等の電着量は、主に電流密度及び電着時間の調整によって制御できる。
電気めっきには、以下に示すめっき条件(1)又はめっき条件(2)が好適に用いられる。
<めっき条件(1)>
液組成 :銅塩10~20g/L、ニッケル塩7~10g/L、
コバルト塩7~10g/L
液温 :30~60℃
電流密度:1~50A/dm2
pH :2.0~3.0
電着時間:0.12~1.15秒
なお、1dm2当たりの各金属の電着量は、銅15~40mg、ニッケル100~1500μg、コバルト700~2500μgが好ましい。
液組成 :銅塩10~20g/L、ニッケル塩7~10g/L、
コバルト塩7~10g/L
液温 :30~60℃
電流密度:1~50A/dm2
pH :2.0~3.0
電着時間:0.12~1.15秒
なお、1dm2当たりの各金属の電着量は、銅15~40mg、ニッケル100~1500μg、コバルト700~2500μgが好ましい。
<めっき条件(2)>
・1次粒子めっき(1)
液組成 :銅塩10~15g/L、ニッケル塩0~10g/L、
コバルト塩0~20g/L、硫酸10~60g/L
液温 :20~40℃
電流密度:10~50A/dm2
電着時間:0.2~5秒
・1次粒子めっき(2)
液組成 :銅塩10~30g/L、硫酸70~120g/L
液温 :30~50℃
電流密度:3~30A/dm2
電着時間:0.2~5秒
・2次粒子めっき
液組成 :銅塩10~20g/L、ニッケル塩0~15g/L、
コバルト塩0~10g/L
液温 :30~40℃
電流密度:10~35A/dm2
電着時間:0.2~5秒
・1次粒子めっき(1)
液組成 :銅塩10~15g/L、ニッケル塩0~10g/L、
コバルト塩0~20g/L、硫酸10~60g/L
液温 :20~40℃
電流密度:10~50A/dm2
電着時間:0.2~5秒
・1次粒子めっき(2)
液組成 :銅塩10~30g/L、硫酸70~120g/L
液温 :30~50℃
電流密度:3~30A/dm2
電着時間:0.2~5秒
・2次粒子めっき
液組成 :銅塩10~20g/L、ニッケル塩0~15g/L、
コバルト塩0~10g/L
液温 :30~40℃
電流密度:10~35A/dm2
電着時間:0.2~5秒
なお、金属箔の表面に対して、ドライエッチング、ウェットエッチング等の粗化処理を施して、その表面の十点平均粗さを上記範囲に調整してもよい。
また、Fポリマーと、金属箔を構成する金属との組み合わせによっては、上記粗化処理を省略しても、F層と金属箔(金属箔層1及び2)との高い接着性が得られる。
さらに、金属箔は、各種特性を向上させる観点から、耐熱処理層、防錆処理層及びクロメート処理層のうちの少なくとも1つの層を備えてもよい。金属箔が積層構成である場合、これらの層は、粗化処理層の基材層と反対側の面、又は粗化処理層と金属箔との間に設けられる。なお、耐熱処理層、防錆処理層又はクロメート処理層の形成には、公知の方法を採用できる。また、耐熱処理層、防錆処理層又はクロメート処理層が金属箔の最外層を構成する場合、その表面が金属箔の表面を構成する。
金属箔の厚さは、積層体の用途に応じて適宜決定され、積層体をプリント配線板に加工して使用する場合には、1~100μmが好ましく、6~30μmがより好ましい。また、極薄の金属箔と、支持金属箔とを積層した積層金属箔を使用する場合、極薄の金属箔の厚さは、2~5μmが好ましい。
また、Fポリマーと、金属箔を構成する金属との組み合わせによっては、上記粗化処理を省略しても、F層と金属箔(金属箔層1及び2)との高い接着性が得られる。
さらに、金属箔は、各種特性を向上させる観点から、耐熱処理層、防錆処理層及びクロメート処理層のうちの少なくとも1つの層を備えてもよい。金属箔が積層構成である場合、これらの層は、粗化処理層の基材層と反対側の面、又は粗化処理層と金属箔との間に設けられる。なお、耐熱処理層、防錆処理層又はクロメート処理層の形成には、公知の方法を採用できる。また、耐熱処理層、防錆処理層又はクロメート処理層が金属箔の最外層を構成する場合、その表面が金属箔の表面を構成する。
金属箔の厚さは、積層体の用途に応じて適宜決定され、積層体をプリント配線板に加工して使用する場合には、1~100μmが好ましく、6~30μmがより好ましい。また、極薄の金属箔と、支持金属箔とを積層した積層金属箔を使用する場合、極薄の金属箔の厚さは、2~5μmが好ましい。
本積層体の製造方法では、金属箔の表面をシランカップリング剤で処理することなく、金属箔の表面にF層を直接接触して形成し、金属箔で構成される金属箔層1の表面に直接接触して設けられたF層を有する本積層体1を製造するか、又は所定量でニッケル原子が存在する金属箔の表面にF層を直接接触して形成し、金属箔で構成される金属箔層2の表面に直接接触して設けられたF層を有する本積層体2を製造する。本積層体の製造方法では、必要に応じて、金属箔の表面にF層を形成するのに先立って、金属箔の表面を上述したようにして粗化処理するのが好ましい。
F層は、金属箔の表面に、Fポリマーのパウダーが溶媒に分散した分散液を付与して加熱する方法、又は金属箔の表面に、Fポリマーを含むフィルムを熱圧着する方法により形成するのが好ましい。
F層は、金属箔の表面に、Fポリマーのパウダーが溶媒に分散した分散液を付与して加熱する方法、又は金属箔の表面に、Fポリマーを含むフィルムを熱圧着する方法により形成するのが好ましい。
金属箔の表面に分散液を付与して加熱する方法では、金属箔の表面に分散液を付与し、分散液が付与された金属箔を加熱すると、分散液から溶媒が除去されるとともに、パウダーの焼成によりF層が形成されて本積層体1及び2が得られる。
分散液を金属箔の表面に付与する方法としては、金属箔の表面に分散液からなる安定した液状被膜(ウェット膜)が形成される方法であればよく、塗布法、液滴吐出法、浸漬法が挙げられ、塗布法が好ましい。塗布法を用いれば、簡単な設備で効率よく金属箔の表面に液状被膜を形成できる。
塗布法としては、スプレー法、ロールコート法、スピンコート法、グラビアコート法、マイクログラビアコート法、グラビアオフセット法、ナイフコート法、キスコート法、バーコート法、ダイコート法、ファウンテンメイヤーバー法、スロットダイコート法が挙げられる。
分散液を金属箔の表面に付与する方法としては、金属箔の表面に分散液からなる安定した液状被膜(ウェット膜)が形成される方法であればよく、塗布法、液滴吐出法、浸漬法が挙げられ、塗布法が好ましい。塗布法を用いれば、簡単な設備で効率よく金属箔の表面に液状被膜を形成できる。
塗布法としては、スプレー法、ロールコート法、スピンコート法、グラビアコート法、マイクログラビアコート法、グラビアオフセット法、ナイフコート法、キスコート法、バーコート法、ダイコート法、ファウンテンメイヤーバー法、スロットダイコート法が挙げられる。
加熱の際は、分散液が付与された金属箔を溶媒の揮発温度で保持して、分散液を乾燥させた後、乾燥被膜を溶媒の揮発温度を上回る温度で保持して、パウダーを焼成するのが好ましい。具体的には、分散液が付与された金属箔を溶媒の沸点以上の温度にて保持した後に、パウダーを焼成するのが好ましい。
「溶媒の揮発温度」は、溶媒の沸点±50℃が好ましく、溶媒の沸点以上の温度がより好ましく、溶媒の沸点+50℃以下の温度がさらに好ましい。乾燥温度は、乾燥雰囲気の温度を意味する。
乾燥時に、溶媒は、必ずしも完全に揮発させる必要はなく、保持後の層形状が安定する程度まで揮発させればよい。具体的には、揮発させるべき溶媒の量は、分散液中に含まれる溶媒のうちの50質量%以上が好ましい。
「溶媒の揮発温度」は、溶媒の沸点±50℃が好ましく、溶媒の沸点以上の温度がより好ましく、溶媒の沸点+50℃以下の温度がさらに好ましい。乾燥温度は、乾燥雰囲気の温度を意味する。
乾燥時に、溶媒は、必ずしも完全に揮発させる必要はなく、保持後の層形状が安定する程度まで揮発させればよい。具体的には、揮発させるべき溶媒の量は、分散液中に含まれる溶媒のうちの50質量%以上が好ましい。
乾燥は、一定温度にて1段階で行ってもよく、異なる温度にて2段階以上で行ってもよい。
乾燥の方法としては、オーブンを用いる方法、通風乾燥炉を用いる方法、赤外線等の熱線を照射する方法が挙げられる。
乾燥は、常圧下および減圧下のいずれの状態で行ってもよい。
また、乾燥雰囲気は、酸化性ガス雰囲気(酸素ガス等)、還元性ガス雰囲気(水素ガス等)、不活性ガス雰囲気(ヘリウムガス、ネオンガス、アルゴンガス、窒素ガス等)のいずれであってもよい。
乾燥温度は、50~280℃が好ましく、120~260℃がより好ましい。乾燥時間は、0.1~30分間が好ましく、0.5~20分間がより好ましい。
以上のような条件で分散液を乾燥すれば、高い生産性を維持しつつ、本積層体1及び2を好適に製造できる。
乾燥の方法としては、オーブンを用いる方法、通風乾燥炉を用いる方法、赤外線等の熱線を照射する方法が挙げられる。
乾燥は、常圧下および減圧下のいずれの状態で行ってもよい。
また、乾燥雰囲気は、酸化性ガス雰囲気(酸素ガス等)、還元性ガス雰囲気(水素ガス等)、不活性ガス雰囲気(ヘリウムガス、ネオンガス、アルゴンガス、窒素ガス等)のいずれであってもよい。
乾燥温度は、50~280℃が好ましく、120~260℃がより好ましい。乾燥時間は、0.1~30分間が好ましく、0.5~20分間がより好ましい。
以上のような条件で分散液を乾燥すれば、高い生産性を維持しつつ、本積層体1及び2を好適に製造できる。
焼成の方法としては、オーブンを用いる方法、通風乾燥炉を用いる方法、赤外線等の熱線を照射する方法が挙げられる。
焼成の方法としては、パウダーを短時間で焼成でき、比較的コンパクトなサイズであるため、遠赤外線を照射する方法が好ましい。また、焼成の方法としては、赤外線加熱と熱風加熱とを組み合わせた方法でもよい。
遠赤外線の有効波長帯は、パウダーの均一な焼成を促すため、2~20μmが好ましく、3~7μmがより好ましい。
なお、得られる本積層体1及び2の表面の平滑性を高めるために、加熱板、加熱ロール等で分散液の乾燥物を加圧してもよい。
焼成の方法としては、パウダーを短時間で焼成でき、比較的コンパクトなサイズであるため、遠赤外線を照射する方法が好ましい。また、焼成の方法としては、赤外線加熱と熱風加熱とを組み合わせた方法でもよい。
遠赤外線の有効波長帯は、パウダーの均一な焼成を促すため、2~20μmが好ましく、3~7μmがより好ましい。
なお、得られる本積層体1及び2の表面の平滑性を高めるために、加熱板、加熱ロール等で分散液の乾燥物を加圧してもよい。
焼成は、常圧下および減圧下のいずれの状態で行ってよい。また、焼成雰囲気は、酸化性ガス雰囲気、還元性ガス雰囲気および不活性ガス雰囲気のいずれであってもよい。ただし、金属箔、形成されるF層それぞれの酸化劣化を抑制する観点から、焼成雰囲気は、還元性ガス雰囲気、不活性ガス雰囲気が好ましい。
焼成温度は、Fポリマーの種類に応じて設定され、180℃~400℃が好ましく、200~380℃がより好ましく、220℃~370℃がさらに好ましい。焼成温度は、焼成雰囲気の温度を意味する。
焼成時間は、30秒~30分間が好ましく、1~15分間がより好ましい。
かかる条件でパウダーを焼成すれば、パウダーの焼成を促進させ、本積層体1及び2の生産性を高めるとともに、Fポリマーの分解によるフッ化水素酸の発生を抑制しやすい。
焼成温度は、Fポリマーの種類に応じて設定され、180℃~400℃が好ましく、200~380℃がより好ましく、220℃~370℃がさらに好ましい。焼成温度は、焼成雰囲気の温度を意味する。
焼成時間は、30秒~30分間が好ましく、1~15分間がより好ましい。
かかる条件でパウダーを焼成すれば、パウダーの焼成を促進させ、本積層体1及び2の生産性を高めるとともに、Fポリマーの分解によるフッ化水素酸の発生を抑制しやすい。
また、パウダーのD50をAとし、金属箔の表面の十点平均粗さをBとしたとき、B/Aは、0.1~1.5が好ましく、0.3~1.3がより好ましい。B/Aが上記範囲であれば、F層の金属箔(金属箔層1及び2)の表面に対するアンカー効果がより顕著に発揮される。
パウダーのD50の具体的な値は、0.05~6μmが好ましく、0.2~3μmがより好ましい。この範囲において、パウダーの流動性と分散性とが良好となり、F層の電気特性(低誘電率等)や耐熱性が最も発現しやすい。
パウダーのD90は、8μm以下が好ましく、5μm以下がより好ましい。この範囲において、パウダーの流動性と分散性とが良好となり、F層の電気特性(低誘電率等)や耐熱性が最も発現しやすい。
また、上記D50及びD90のパウダーであれば、F層の金属箔(金属箔層1及び2)の表面に対するアンカー効果がより生じやすい。
パウダーの疎充填嵩密度は、0.05g/mL以上が好ましく、0.08~0.5g/mLがより好ましい。パウダーの密充填嵩密度は、0.05g/mL以上が好ましく、0.1~0.8g/mLがより好ましい。疎充填嵩密度又は密充填嵩密度が上記範囲にある場合、パウダーのハンドリング性が優れる。
パウダーのD50の具体的な値は、0.05~6μmが好ましく、0.2~3μmがより好ましい。この範囲において、パウダーの流動性と分散性とが良好となり、F層の電気特性(低誘電率等)や耐熱性が最も発現しやすい。
パウダーのD90は、8μm以下が好ましく、5μm以下がより好ましい。この範囲において、パウダーの流動性と分散性とが良好となり、F層の電気特性(低誘電率等)や耐熱性が最も発現しやすい。
また、上記D50及びD90のパウダーであれば、F層の金属箔(金属箔層1及び2)の表面に対するアンカー効果がより生じやすい。
パウダーの疎充填嵩密度は、0.05g/mL以上が好ましく、0.08~0.5g/mLがより好ましい。パウダーの密充填嵩密度は、0.05g/mL以上が好ましく、0.1~0.8g/mLがより好ましい。疎充填嵩密度又は密充填嵩密度が上記範囲にある場合、パウダーのハンドリング性が優れる。
Fポリマーのパウダー粒子は、Fポリマーからなるのが好ましい。パウダー粒子におけるFポリマーの含有量は、80質量%以上が好ましく、100質量%がより好ましい。
パウダー粒子に含まれ得る他の成分としては、芳香族ポリエステル、ポリアミドイミド、熱可塑性ポリイミド、ポリフェニレンエーテル、ポリフェニレンオキシドが挙げられる。
パウダー粒子に含まれ得る他の成分としては、芳香族ポリエステル、ポリアミドイミド、熱可塑性ポリイミド、ポリフェニレンエーテル、ポリフェニレンオキシドが挙げられる。
分散液における溶媒は、25℃で液体の化合物であり、水性溶媒であってもよく、非水性溶媒であってもよい。
溶媒は、水、アミド、アルコール、スルホキシド、エステル、ケトン又はグリコールエーテルが好ましく、水、ケトン又はアミドがより好ましく、ケトン又はアミドがさらに好ましい。溶媒は、1種を単独で使用してもよく、2種以上を併用してもよい。
溶媒の具体例としては、水、メタノール、エタノール、イソプロパノール、N,N-ジメチルホルムアミド、N,N-ジメチルアセトアミド、N-メチル-2-ピロリドン、ジメチルスルホキシド、ジエチルエーテル、ジオキサン、乳酸エチル、酢酸エチル、酢酸ブチル、メチルエチルケトン、メチルイソプロピルケトン、シクロペンタノン、シクロヘキサノン、エチレングリコールモノイソプロピルエーテル、セロソルブ(メチルセロソルブ、エチルセロソルブ等)が挙げられる。
溶媒は、金属箔の表面とFポリマーとの濡れ性を増し、金属箔の表面の水酸基及び/又は金属原子とFポリマーが有する酸素含有極性基とをより良好に相互作用させる観点から、極性溶媒が好ましく、水、アミド又はケトンが好ましく、水、N,N-ジメチルアセトアミド、N-メチル-2-ピロリドン、シクロヘキサノン又はメチルエチルケトンがより好ましい。
溶媒は、水、アミド、アルコール、スルホキシド、エステル、ケトン又はグリコールエーテルが好ましく、水、ケトン又はアミドがより好ましく、ケトン又はアミドがさらに好ましい。溶媒は、1種を単独で使用してもよく、2種以上を併用してもよい。
溶媒の具体例としては、水、メタノール、エタノール、イソプロパノール、N,N-ジメチルホルムアミド、N,N-ジメチルアセトアミド、N-メチル-2-ピロリドン、ジメチルスルホキシド、ジエチルエーテル、ジオキサン、乳酸エチル、酢酸エチル、酢酸ブチル、メチルエチルケトン、メチルイソプロピルケトン、シクロペンタノン、シクロヘキサノン、エチレングリコールモノイソプロピルエーテル、セロソルブ(メチルセロソルブ、エチルセロソルブ等)が挙げられる。
溶媒は、金属箔の表面とFポリマーとの濡れ性を増し、金属箔の表面の水酸基及び/又は金属原子とFポリマーが有する酸素含有極性基とをより良好に相互作用させる観点から、極性溶媒が好ましく、水、アミド又はケトンが好ましく、水、N,N-ジメチルアセトアミド、N-メチル-2-ピロリドン、シクロヘキサノン又はメチルエチルケトンがより好ましい。
分散液は、さらにフッ素系分散剤を含むのが好ましい。フッ素系分散剤は、パウダー粒子の表面に化学的及び/又は物理的に吸着して、パウダー粒子を溶媒に安定的に分散させる機能を有する化合物である。かかるフッ素系分散剤を含む分散液では、パウダーの分散性がより向上し、金属箔の表面とFポリマーとの濡れ性が増し、金属箔の表面の酸化物及び/又は金属原子とFポリマーが有する酸素含有極性基とが高度に相互作用しやすい。
フッ素系分散剤は、フッ素原子を含有する疎水部位と親水部位とを有する化合物(界面活性剤)が好ましく、フルオロポリオール、フルオロシリコーン又はフルオロポリエーテルがより好ましく、フルオロポリオールがさらに好ましい。
また、フッ素系分散剤は、ノニオン性のポリマー状化合物が好ましい。
かかるフッ素系分散剤は、上記溶媒との相互作用が高く、よって分散液の塗膜形成性(チキソ比、接着性、透明性等)が向上しやすい。
フッ素系分散剤は、フッ素原子を含有する疎水部位と親水部位とを有する化合物(界面活性剤)が好ましく、フルオロポリオール、フルオロシリコーン又はフルオロポリエーテルがより好ましく、フルオロポリオールがさらに好ましい。
また、フッ素系分散剤は、ノニオン性のポリマー状化合物が好ましい。
かかるフッ素系分散剤は、上記溶媒との相互作用が高く、よって分散液の塗膜形成性(チキソ比、接着性、透明性等)が向上しやすい。
フルオロポリオールとは、Fポリマーと異なり、水酸基とフッ素原子とを有するポリマー状ポリオールである。また、ポリマー状ポリオールは、水酸基の一部が化学修飾され、変性されてもよい。
フルオロポリオールとしては、エチレン性不飽和モノマーに由来する炭素鎖からなる主鎖と、この主鎖から分岐する側鎖として、含フッ素炭化水素基と水酸基とを有する化合物が挙げられる。
かかるフルオロポリオールを含む分散液を使用した場合、分散液を付与し加熱する際のフルオロポリオールの分解物が、金属箔の表面に酸化物を形成させ易く、金属箔(金属箔層1及び2)とポリマー層とをより強固に接着させやすい。
フルオロポリオールとしては、エチレン性不飽和モノマーに由来する炭素鎖からなる主鎖と、この主鎖から分岐する側鎖として、含フッ素炭化水素基と水酸基とを有する化合物が挙げられる。
かかるフルオロポリオールを含む分散液を使用した場合、分散液を付与し加熱する際のフルオロポリオールの分解物が、金属箔の表面に酸化物を形成させ易く、金属箔(金属箔層1及び2)とポリマー層とをより強固に接着させやすい。
フルオロポリオールは、ポリフルオロアルキル基又はポリフルオロアルケニル基を有する含フッ素(メタ)アクリレートに基づく単位と、ポリオキシアルキレン基又はヒドロキシアルキル基を有する親水性(メタ)アクリレートに基づく単位とを含むコポリマーが好ましい。なお、(メタ)アクリレートとは、アクリレート、メタクリレート及びアクリレートのα位の水素原子が他の原子又は原子団で置換されたアクリレート誘導体の総称である。
含フッ素(メタ)アクリレートの具体例としては、CH2=CHCOO(CH2)2(CF2)4F、CH2=C(CH3)COO(CH2)2(CF2)4F、CH2=CClCOO(CH2)2(CF2)4F、CH2=CHCOO(CH2)2(CF2)6F、CH2=C(CH3)COO(CH2)2(CF2)6F、CH2=CHCOO(CH2)4OCF(CF3)(C(CF(CF3)2)(=C(CF3)2)、CH2=CHCOO(CH2)4OC(CF3)(=C(CF(CF3)2)(CF(CF3)2)、CH2=C(CH3)COO(CH2)2NHCOOCH(CH2OCH2CH2(CF2)6F)2、CH2=C(CH3)COO(CH2)2NHCOOCH(CH2OCH2(CF2)6F)2、CH2=C(CH3)COO(CH2)3NHCOOCH(CH2OCH2(CF2)6F)2が挙げられる。
親水性(メタ)アクリレートの具体例としては、CH2=CHCOO(CH2)2OH、CH2=C(CH3)COO(CH2)2OH、CH2=CHCOO(CH2)2(OCH2CH2)10OH、CH2=CHCOO(CH2)4(OCH2CH2)10OH、CH2=C(CH3)COO(CH2)2(OCH2CH2)10OH、H2=C(CH3)COO(CH2)4(OCH2CH2)10OH、CH2=CHCOO(CH2)2(OCH2CH(CH3))10OH、CH2=C(CH3)COO(CH2)2(OCH2CH(CH3))10OH、CH2=CHCOO(CH2)2(OCH2CH2)23OH、CH2=C(CH3)COO(CH2)2(OCH2CH2)23OHが挙げられる。
フルオロポリオールは、含フッ素(メタ)アクリレートに基づく単位と親水性(メタ)アクリレートに基づく単位とのみを含んでもよく、さらに他の単位を含んでもよい。
フルオロポリオールのフッ素含有量は、10~45質量%が好ましく、15~40質量%がより好ましい。
また、フルオロポリオールの重量平均分子量は、2000~80000が好ましく、6000~20000がより好ましい。
フルオロポリオールのフッ素含有量は、10~45質量%が好ましく、15~40質量%がより好ましい。
また、フルオロポリオールの重量平均分子量は、2000~80000が好ましく、6000~20000がより好ましい。
フルオロシリコーンとしては、側鎖の一部にC-F結合を含むポリオルガノシロキサンが挙げられる。
また、フルオロポリエーテルとしては、ポリオキシアルキレンアルキルエーテルの水素原子の一部がフッ素原子に置換された化合物が挙げられる。なお、フルオロポリエーテルには、上記化合物のモノオール体も包含される。
また、フルオロポリエーテルとしては、ポリオキシアルキレンアルキルエーテルの水素原子の一部がフッ素原子に置換された化合物が挙げられる。なお、フルオロポリエーテルには、上記化合物のモノオール体も包含される。
さらに、分散液は、他の材料を含んでいてもよい。他の材料は、分散液に溶解してもよく、溶解しなくてもよい。
かかる他の材料は、非硬化性樹脂であってもよく、硬化性樹脂であってもよい。
非硬化性樹脂としては、熱溶融性樹脂、非溶融性樹脂が挙げられる。熱溶融性樹脂としては、熱可塑性ポリイミドが挙げられる。非溶融性樹脂としては、硬化性樹脂の硬化物等が挙げられる。
かかる他の材料は、非硬化性樹脂であってもよく、硬化性樹脂であってもよい。
非硬化性樹脂としては、熱溶融性樹脂、非溶融性樹脂が挙げられる。熱溶融性樹脂としては、熱可塑性ポリイミドが挙げられる。非溶融性樹脂としては、硬化性樹脂の硬化物等が挙げられる。
硬化性樹脂としては、反応性基を有するポリマー、反応性基を有するオリゴマー、低分子化合物、反応性基を有する低分子化合物が挙げられる。反応性基としては、カルボニル基含有基、ヒドロキシ基、アミノ基、エポキシ基が挙げられる。
硬化性樹脂は、エポキシ樹脂、熱硬化性ポリイミド、ポリイミド前駆体であるポリアミック酸、アクリル樹脂、フェノール樹脂、ポリエステル樹脂、ポリオレフィン樹脂、変性ポリフェニレンエーテル樹脂、多官能シアン酸エステル樹脂、多官能マレイミド-シアン酸エステル樹脂、多官能性マレイミド樹脂、ビニルエステル樹脂、尿素樹脂、ジアリルフタレート樹脂、メラニン樹脂、グアナミン樹脂、メラミン-尿素共縮合樹脂が挙げられる。
硬化性樹脂は、エポキシ樹脂、熱硬化性ポリイミド、ポリイミド前駆体であるポリアミック酸、アクリル樹脂、フェノール樹脂、ポリエステル樹脂、ポリオレフィン樹脂、変性ポリフェニレンエーテル樹脂、多官能シアン酸エステル樹脂、多官能マレイミド-シアン酸エステル樹脂、多官能性マレイミド樹脂、ビニルエステル樹脂、尿素樹脂、ジアリルフタレート樹脂、メラニン樹脂、グアナミン樹脂、メラミン-尿素共縮合樹脂が挙げられる。
エポキシ樹脂の具体例としては、各型のエポキシ樹脂(ナフタレン型、クレゾールノボラック型、ビスフェノールA型、ビスフェノールF型、ビスフェノールS型、脂環式型、脂肪族鎖状型、クレゾールノボラック型、フェノールノボラック型、アルキルフェノールノボラック型、アラルキル型、ビフェノール型等)が挙げられる。
ビスマレイミド樹脂としては、特開平7-70315号公報に記載される樹脂組成物(BTレジン)、国際公開第2013/008667号に記載される樹脂が挙げられる。
ポリアミック酸は、通常、Fポリマーが有する酸素含有極性基と反応し得る反応性基を有している。
ポリアミック酸を形成するジアミン、多価カルボン酸二無水物としては、特許第5766125号公報の[0020]、特許第5766125号公報の[0019]、特開2012-145676号公報の[0055]、[0057]等に記載の化合物が挙げられる。
ビスマレイミド樹脂としては、特開平7-70315号公報に記載される樹脂組成物(BTレジン)、国際公開第2013/008667号に記載される樹脂が挙げられる。
ポリアミック酸は、通常、Fポリマーが有する酸素含有極性基と反応し得る反応性基を有している。
ポリアミック酸を形成するジアミン、多価カルボン酸二無水物としては、特許第5766125号公報の[0020]、特許第5766125号公報の[0019]、特開2012-145676号公報の[0055]、[0057]等に記載の化合物が挙げられる。
熱溶融性樹脂としては、熱可塑性ポリイミド等の熱可塑性樹脂、硬化性樹脂の熱溶融性の硬化物が挙げられる。
熱可塑性樹脂としては、ポリエステル樹脂、ポリオレフィン樹脂、スチレン樹脂、ポリカーボネート、熱可塑性ポリイミド、ポリアリレート、ポリスルホン、ポリアリルスルホン、芳香族ポリアミド、芳香族ポリエーテルアミド、ポリフェニレンスルファイド、ポリアリルエーテルケトン、ポリアミドイミド、液晶性ポリエステル、ポリフェニレンエーテルが挙げられ、熱可塑性ポリイミド、液晶性ポリエステル又はポリフェニレンエーテルが好ましい。
また、かかる他の材料としては、チキソ性付与剤、消泡剤、無機フィラー、反応性アルコキシシラン、脱水剤、可塑剤、耐候剤、酸化防止剤、熱安定剤、滑剤、帯電防止剤、増白剤、着色剤、導電剤、離型剤、表面処理剤、粘度調節剤、難燃剤も挙げられる。
熱可塑性樹脂としては、ポリエステル樹脂、ポリオレフィン樹脂、スチレン樹脂、ポリカーボネート、熱可塑性ポリイミド、ポリアリレート、ポリスルホン、ポリアリルスルホン、芳香族ポリアミド、芳香族ポリエーテルアミド、ポリフェニレンスルファイド、ポリアリルエーテルケトン、ポリアミドイミド、液晶性ポリエステル、ポリフェニレンエーテルが挙げられ、熱可塑性ポリイミド、液晶性ポリエステル又はポリフェニレンエーテルが好ましい。
また、かかる他の材料としては、チキソ性付与剤、消泡剤、無機フィラー、反応性アルコキシシラン、脱水剤、可塑剤、耐候剤、酸化防止剤、熱安定剤、滑剤、帯電防止剤、増白剤、着色剤、導電剤、離型剤、表面処理剤、粘度調節剤、難燃剤も挙げられる。
分散液の粘度は、50~10000mPa・sが好ましく、75~1000mPa・sがより好ましく、100~500mPa・sがさらに好ましい。この場合、分散液の分散性に優れるだけでなく、その塗工性や異種の樹脂材料のワニスとの相溶性にも優れている。
また、分散液のチキソ比は、1.0~2.2が好ましく、1.4~2.2がより好ましく、1.5~2.0がさらに好ましい。この場合、分散液の分散性に優れるだけでなく、F層の均質性が向上しやすい。なお、チキソ比は、回転数が30rpmの条件で測定される分散液の粘度を、回転数が60rpmの条件で測定される分散液の粘度で除して算出される。
また、分散液のチキソ比は、1.0~2.2が好ましく、1.4~2.2がより好ましく、1.5~2.0がさらに好ましい。この場合、分散液の分散性に優れるだけでなく、F層の均質性が向上しやすい。なお、チキソ比は、回転数が30rpmの条件で測定される分散液の粘度を、回転数が60rpmの条件で測定される分散液の粘度で除して算出される。
金属箔の表面にFポリマーを含むフィルムを熱圧着する方法では、金属箔の表面にFポリマーを含むフィルムを熱圧着すると、F層が形成されて、金属箔で構成される金属箔層1及び2の表面に直接接触して設けられたF層を有する本積層体1及び2が得られる。
フィルムは、Fポリマー自体、又はFポリマーを含む組成物を、押出成形法、インフレーション成形法等によってフィルム状に成形する方法により作製できる。
積層体の製造は、具体的には、金属箔の表面にフィルムを重ね合わせた仮積層体を、搬送しながら厚み方向(積層方向)に加圧せずに加熱する予備加熱工程と、仮積層体を加熱しながら厚み方向(積層方向)に加圧して貼り合わせる熱圧着工程とを経て行われる。
仮積層体では、金属箔とフィルムとが互いに密着した状態であるが、未だ接着(圧着)されていない状態である。
フィルムは、Fポリマー自体、又はFポリマーを含む組成物を、押出成形法、インフレーション成形法等によってフィルム状に成形する方法により作製できる。
積層体の製造は、具体的には、金属箔の表面にフィルムを重ね合わせた仮積層体を、搬送しながら厚み方向(積層方向)に加圧せずに加熱する予備加熱工程と、仮積層体を加熱しながら厚み方向(積層方向)に加圧して貼り合わせる熱圧着工程とを経て行われる。
仮積層体では、金属箔とフィルムとが互いに密着した状態であるが、未だ接着(圧着)されていない状態である。
なお、仮積層体を形成する前に、フィルムには、100℃以上250℃未満(好ましくは180℃以上250℃未満)の温度で予め加熱処理を施してもよい。予め加熱処理を施しておけば、予備加熱工程および熱圧着工程におけるフィルムの収縮を小さくでき、その結果、積層体の反りを低減できる。
また、仮積層体を形成する前に、フィルムの表面(金属箔側の表面)には、コロナ放電処理、プラズマ処理等の表面処理を施してもよい。予め表面処理を施せば、フィルムの表面に存在する酸素含有極性基の数を増大でき、得られる積層体において、F層の金属箔層1及び2に対する接着強度をより高められる。
また、仮積層体を形成する前に、フィルムの表面(金属箔側の表面)には、コロナ放電処理、プラズマ処理等の表面処理を施してもよい。予め表面処理を施せば、フィルムの表面に存在する酸素含有極性基の数を増大でき、得られる積層体において、F層の金属箔層1及び2に対する接着強度をより高められる。
予備加熱工程では、仮積層体を、後段の熱圧着工程で圧着する前に、その積層方向(厚み方向)に加圧せずに予備加熱手段で加熱する。
予備加熱手段は、仮積層体に熱源を接触させる接触方式でもよく、非接触で仮積層体を加熱する非接触方式でもよい。金属箔とフィルムとを互いに密着させやすい点で、予備加熱手段は、接触方式が好ましい。具体的には、加熱された金属ロールに仮積層体を接触させた状態で搬送する方式が好ましい。
熱圧着工程において加圧される直前の仮積層体の温度(予備加熱の温度)は、Fポリマーの溶融温度より20℃低い温度以上が好ましく、Fポリマーの溶融温度以上がさらに好ましい。予備加熱の温度は、熱圧着の温度以下が好ましい。予備加熱の温度が上記の範囲であると、フィルムの収縮や切れを良好に防止できる。
予備加熱手段は、仮積層体に熱源を接触させる接触方式でもよく、非接触で仮積層体を加熱する非接触方式でもよい。金属箔とフィルムとを互いに密着させやすい点で、予備加熱手段は、接触方式が好ましい。具体的には、加熱された金属ロールに仮積層体を接触させた状態で搬送する方式が好ましい。
熱圧着工程において加圧される直前の仮積層体の温度(予備加熱の温度)は、Fポリマーの溶融温度より20℃低い温度以上が好ましく、Fポリマーの溶融温度以上がさらに好ましい。予備加熱の温度は、熱圧着の温度以下が好ましい。予備加熱の温度が上記の範囲であると、フィルムの収縮や切れを良好に防止できる。
予備加熱工程では、仮積層体を連続的に加熱してもよく、断続的に加熱してもよい。搬送中の仮積層体に対して予備加熱が開始される位置から、仮積層体が熱圧着工程において加圧される直前までの搬送時間(予備加熱の時間)は、10~30秒間が好ましい。予備加熱の時間が上記範囲であると、フィルムの収縮や切れを良好に防止しつつ、得られる積層体においては、F層の金属箔層1及び2に対する接着力が高まる。
予備加熱工程を接触方式の予備加熱手段で行う場合、予備加熱の時間が上記範囲であれば、仮積層体の温度は、この仮積層体に接触させる熱源の表面温度と同じ温度になる。
予備加熱工程を接触方式の予備加熱手段で行う場合、予備加熱の時間が上記範囲であれば、仮積層体の温度は、この仮積層体に接触させる熱源の表面温度と同じ温度になる。
熱圧着工程は、一対以上の熱圧着手段を備えた熱圧着装置等を用いて連続的に行われることが好ましい。熱圧着手段とは、上記仮積層体を加熱しながら加圧することによって圧着する手段を意味する。熱圧着手段として一対以上の金属ロールを備えた熱ロール圧着装置が好適に用いられる。
熱ロール圧着装置では、仮積層体が、所定の温度に加熱された一対の金属ロールの間を通過する際に、金属ロールとの接触により加熱されるとともに、厚さ方向の加圧力を受けて、フィルムが金属箔に圧着される。仮積層体が、複数対の金属ロールを順に通過する構成としてもよい。
熱ロール圧着装置では、仮積層体が、所定の温度に加熱された一対の金属ロールの間を通過する際に、金属ロールとの接触により加熱されるとともに、厚さ方向の加圧力を受けて、フィルムが金属箔に圧着される。仮積層体が、複数対の金属ロールを順に通過する構成としてもよい。
仮積層体を加圧する金属ロールの表面温度(熱圧着の温度)は、Fポリマーの溶融温度以上が好ましく、400℃以上がより好ましい。この場合、F層の金属箔層1及び2に対する良好な接着強度が得られ剥離が生じにくい。
仮積層体を加圧する一対の金属ロール間の圧力(熱圧着の圧力)は、ロールの1cm幅あたりに付加される荷重で表されるロール線圧で、98~1470N/cmが好ましい。この場合、熱圧着時にフィルムが切れにくく、F層の金属箔層1及び2に対する良好な接着強度が得られ剥離が生じにくい。
仮積層体を加圧する一対の金属ロール間の圧力(熱圧着の圧力)は、ロールの1cm幅あたりに付加される荷重で表されるロール線圧で、98~1470N/cmが好ましい。この場合、熱圧着時にフィルムが切れにくく、F層の金属箔層1及び2に対する良好な接着強度が得られ剥離が生じにくい。
仮積層体が一対の金属ロール間を通過する際の走行速度(熱圧着の速度)は、0.5m/分以上が好ましく、1m/分以上がより好ましい。この場合、充分に熱圧着が可能であり、本積層体1及び2の生産性も一層向上できる。熱圧着の速度は、8m/分以下が好ましい。この場合、F層と金属箔層1及び2を強固に接着させやすい。
フィルムは、Fポリマーを含むフィルム(基材フィルム)の金属箔と反対側の面に耐熱性樹脂フィルムを有する積層フィルムであってもよい。
耐熱性樹脂フィルムは、耐熱性樹脂を含み、必要に応じて添加剤等を含んでもよい。
耐熱性樹脂フィルム中の耐熱性樹脂の含有量は、耐熱性樹脂フィルムの耐熱性を高める観点から、50質量%以上が好ましく、80質量%以上がより好ましい。
耐熱性樹脂フィルムは、耐熱性樹脂を含み、必要に応じて添加剤等を含んでもよい。
耐熱性樹脂フィルム中の耐熱性樹脂の含有量は、耐熱性樹脂フィルムの耐熱性を高める観点から、50質量%以上が好ましく、80質量%以上がより好ましい。
耐熱性樹脂としては、ポリイミド(芳香族ポリイミド等)、ポリアリレート、ポリスルホン、ポリアリルスルホン(ポリエーテルスルホン等)、芳香族ポリアミド、芳香族ポリエーテルアミド、ポリフェニレンスルファイド、ポリアリルエーテルケトン、ポリアミドイミド、液晶ポリエステルが挙げられる。
耐熱性樹脂は、より高い耐熱性が得られやすい点で熱硬化性樹脂が好ましい。
熱硬化性樹脂としては、熱硬化性ポリイミド、エポキシ樹脂、アクリル樹脂が挙げられる。積層体の電気特性を向上させる観点からは、熱硬化性樹脂としては、熱硬化性ポリイミドが好ましい。
熱硬化性ポリイミドとしては、芳香族ポリイミドが好ましく、芳香族ジカルボン酸と芳香族ジアミンとの重縮合で製造される全芳香族ポリイミドがより好ましい。
耐熱性樹脂は、より高い耐熱性が得られやすい点で熱硬化性樹脂が好ましい。
熱硬化性樹脂としては、熱硬化性ポリイミド、エポキシ樹脂、アクリル樹脂が挙げられる。積層体の電気特性を向上させる観点からは、熱硬化性樹脂としては、熱硬化性ポリイミドが好ましい。
熱硬化性ポリイミドとしては、芳香族ポリイミドが好ましく、芳香族ジカルボン酸と芳香族ジアミンとの重縮合で製造される全芳香族ポリイミドがより好ましい。
添加剤としては、比誘電率及び誘電正接が低い無機フィラーが好ましい。
かかる無機フィラーとしては、シリカ、クレー、タルク、炭酸カルシウム、マイカ、珪藻土、アルミナ、酸化亜鉛、酸化チタン、酸化カルシウム、酸化マグネシウム、酸化鉄、酸化錫、酸化アンチモン、水酸化カルシウム、水酸化マグネシウム、水酸化アルミニウム、塩基性炭酸マグネシウム、炭酸マグネシウム、炭酸亜鉛、炭酸バリウム、ドーソナイト、ハイドロタルサイト、硫酸カルシウム、硫酸バリウム、珪酸カルシウム、モンモリロナイト、ベントナイト、活性白土、セピオライト、イモゴライト、セリサイト、ガラス繊維、ガラスビーズ、シリカ系バルーン、カーボンブラック、カーボンナノチューブ、カーボンナノホーン、グラファイト、炭素繊維、ガラスバルーン、炭素バーン、木粉、ホウ酸亜鉛が挙げられる。なお、無機フィラーは、1種を単独で用いてもよく、2種以上を併用してもよい。
かかる無機フィラーとしては、シリカ、クレー、タルク、炭酸カルシウム、マイカ、珪藻土、アルミナ、酸化亜鉛、酸化チタン、酸化カルシウム、酸化マグネシウム、酸化鉄、酸化錫、酸化アンチモン、水酸化カルシウム、水酸化マグネシウム、水酸化アルミニウム、塩基性炭酸マグネシウム、炭酸マグネシウム、炭酸亜鉛、炭酸バリウム、ドーソナイト、ハイドロタルサイト、硫酸カルシウム、硫酸バリウム、珪酸カルシウム、モンモリロナイト、ベントナイト、活性白土、セピオライト、イモゴライト、セリサイト、ガラス繊維、ガラスビーズ、シリカ系バルーン、カーボンブラック、カーボンナノチューブ、カーボンナノホーン、グラファイト、炭素繊維、ガラスバルーン、炭素バーン、木粉、ホウ酸亜鉛が挙げられる。なお、無機フィラーは、1種を単独で用いてもよく、2種以上を併用してもよい。
本積層体1及び2において、F層の金属箔層1及び2に対する剥離強度は、10N/cm以上が好ましく、15N/cm以上がより好ましい。なお、剥離強度の上限は、通常、20N/cmである。
本積層体1及び2の反り率は、25%以下が好ましく、7%以下がより好ましい。この場合、本積層体1及び2をプリント配線板に加工する際のハンドリング性と、得られるプリント配線板の伝送特性とが優れる。
本積層体1及び2の寸法変化率は、±1%以下が好ましく、±0.2%以下がより好ましい。この場合、本積層体1及び2をプリント配線板に加工し、さらにそれを多層化しやすい。
本積層体1及び2の反り率は、25%以下が好ましく、7%以下がより好ましい。この場合、本積層体1及び2をプリント配線板に加工する際のハンドリング性と、得られるプリント配線板の伝送特性とが優れる。
本積層体1及び2の寸法変化率は、±1%以下が好ましく、±0.2%以下がより好ましい。この場合、本積層体1及び2をプリント配線板に加工し、さらにそれを多層化しやすい。
F層の表面の水接触角は、70~100°が好ましく、70~90°がより好ましい。この場合、F層と他の基板との接着性がより優れる。上記範囲が下限以上であれば、本積層体1及び2をプリント配線板に加工した際の電気特性がより優れる。
F層の厚さは、1~50μmが好ましく、5~15μmがより好ましい。この範囲において、本積層体1及び2をプリント配線板に加工した際の電気特性と積層体の反り抑制効果とをバランスさせやすい。
なお、本積層体1及び2が金属箔層1及び2の両面にF層を有する場合、それぞれのF層の組成及び厚さは、本積層体1及び2の反りを抑制する点から、それぞれ同じであることが好ましい。
F層の厚さは、1~50μmが好ましく、5~15μmがより好ましい。この範囲において、本積層体1及び2をプリント配線板に加工した際の電気特性と積層体の反り抑制効果とをバランスさせやすい。
なお、本積層体1及び2が金属箔層1及び2の両面にF層を有する場合、それぞれのF層の組成及び厚さは、本積層体1及び2の反りを抑制する点から、それぞれ同じであることが好ましい。
F層の比誘電率は、1.98以下が好ましく、1.95以下がより好ましい。F層の比誘電率の下限は、通常、1.50である。
F層の誘電正接は、0.0024以下が好ましく、0.0019以下がより好ましい。F層の比誘電率の下限は、通常、0.0005である。
この場合、低誘電率が求められるプリント配線板等に本積層体1及び2を好適に使用できる。
なお、F層の比誘電率及び誘電正接は、測定器としてネットワークアナライザを使用して、空洞共振器摂動法により、測定周波数10GHzで測定される値である。
F層の誘電正接は、0.0024以下が好ましく、0.0019以下がより好ましい。F層の比誘電率の下限は、通常、0.0005である。
この場合、低誘電率が求められるプリント配線板等に本積層体1及び2を好適に使用できる。
なお、F層の比誘電率及び誘電正接は、測定器としてネットワークアナライザを使用して、空洞共振器摂動法により、測定周波数10GHzで測定される値である。
本積層体1及び2は、プリント配線板に加工できる。
例えば、本積層体1及び2の金属箔層1及び2をエッチング等によって所定のパターンの導体回路(パターン回路)に加工する方法や、本積層体1及び2を電解めっき法(セミアディティブ法(SAP法)、モディファイドセミアディティブ法(MSAP法)等)によってパターン回路に加工する方法を使用すれば、本積層体1及び2からプリント配線板を製造できる。
プリント配線板の製造においては、パターン回路を形成した後に、パターン回路上に層間絶縁膜を形成し、層間絶縁膜上にさらに導体回路を形成してもよい。層間絶縁膜は、上記分散液によって形成してもよい。
プリント配線板の製造においては、パターン回路上にソルダーレジストを積層してもよい。ソルダーレジストは、上記分散液によって形成してもよい。
プリント配線板の製造においては、パターン回路上にカバーレイフィルムを積層してもよい。カバーレイフィルムは、上記分散液によって形成してもよい。
例えば、本積層体1及び2の金属箔層1及び2をエッチング等によって所定のパターンの導体回路(パターン回路)に加工する方法や、本積層体1及び2を電解めっき法(セミアディティブ法(SAP法)、モディファイドセミアディティブ法(MSAP法)等)によってパターン回路に加工する方法を使用すれば、本積層体1及び2からプリント配線板を製造できる。
プリント配線板の製造においては、パターン回路を形成した後に、パターン回路上に層間絶縁膜を形成し、層間絶縁膜上にさらに導体回路を形成してもよい。層間絶縁膜は、上記分散液によって形成してもよい。
プリント配線板の製造においては、パターン回路上にソルダーレジストを積層してもよい。ソルダーレジストは、上記分散液によって形成してもよい。
プリント配線板の製造においては、パターン回路上にカバーレイフィルムを積層してもよい。カバーレイフィルムは、上記分散液によって形成してもよい。
本発明の複合積層体(本複合体)の製造方法は、所定の積層体(F層付金属箔)が有する金属箔層の少なくとも一部を除去し、露出したポリマー層にプリプレグを接着させ、少なくともポリマー層とプリプレグ層とが積層された複合積層体を得る方法である。
金属箔層の全てを除去すれば、ポリマー層とプリプレグ層とを有する2層構成の複合積層体が得られる。また、金属箔層の一部を除去して回路パターンを形成すれば、ポリマー層と、プリプレグ層と、これらに挟持された回路パターンとを有する3層構成の複合積層体が得られる。後者の複合積層体は、プリント配線板として好適に使用できる。
複合積層体の製造に使用される積層体は、十点平均粗さが0.1μm以上の表面を有する金属箔層と、その表面に積層されたF層とを備えている。
金属箔層の全てを除去すれば、ポリマー層とプリプレグ層とを有する2層構成の複合積層体が得られる。また、金属箔層の一部を除去して回路パターンを形成すれば、ポリマー層と、プリプレグ層と、これらに挟持された回路パターンとを有する3層構成の複合積層体が得られる。後者の複合積層体は、プリント配線板として好適に使用できる。
複合積層体の製造に使用される積層体は、十点平均粗さが0.1μm以上の表面を有する金属箔層と、その表面に積層されたF層とを備えている。
金属箔層の表面は、十点平均粗さが0.1μm以上であり、微小な凹凸が不規則に存在している。この表面に形成されたF層は、金属箔層との接触面に、金属箔層の表面形状が転写される。このため、金属箔層の除去により露出するF層の接触面には、金属箔層の表面形状に対応する微小な凹凸が不規則に存在する。
本発明では、かかる表面性状の接触面にプリプレグを接着させて複合積層体を得るため、プリプレグのF層の接触面に対する高いアンカー効果が生じると考えられる。その結果、F層とプリプレグ層との間に高い接着力(剥離強度)が発現したと推察される。
以上のような効果は、後述する本発明の好ましい態様において、顕著に発現する。
本発明では、かかる表面性状の接触面にプリプレグを接着させて複合積層体を得るため、プリプレグのF層の接触面に対する高いアンカー効果が生じると考えられる。その結果、F層とプリプレグ層との間に高い接着力(剥離強度)が発現したと推察される。
以上のような効果は、後述する本発明の好ましい態様において、顕著に発現する。
本複合体の製造方法におけるFポリマーの態様は、好適な態様も含めて、本積層体におけるFポリマーのそれと同様である。
本複合体の製造方法における金属箔層を構成する金属の態様は、好適な態様も含めて、本積層体における金属箔層を構成する金属のそれと同様である。
本複合体の製造方法における金属箔層を構成する金属の態様は、好適な態様も含めて、本積層体における金属箔層を構成する金属のそれと同様である。
本複合体の製造方法における金属箔層の表面の十点平均粗さは、0.1μm以上であり、0.3μm以上が好ましい。上記十点平均粗さは、7μm以下が好ましく、2.5μm以下がより好ましく、2μm以下がさらに好ましい。また、上記範囲の十点平均粗さであれば、金属箔層の表面の凹凸の程度が大き過ぎないため、本複合体をプリント配線板に加工した場合でも、伝送損失の増大を抑制できる。また、プリプレグを積層した場合に、プリプレグのマトリックス樹脂とFポリマーが相溶化して、層間の接着力がより向上しやすい。
本複合体の製造方法における金属箔層が粗化処理層を有する場合、その表面の十点平均粗さは、金属粒子のサイズ、金属粒子の数等の設定により調整できる。
粗化処理層は、基材層を陰極とした電気めっき法により、金属粒子を基材層上に析出(電着)して形成されるのが好ましい。この場合、金属粒子のサイズ、金属粒子の数等の電着量は、主に電流密度及び電着時間の調整によって制御できる。
電気めっきの条件は、本積層体における電気めっきの条件と同じ条件を採用できる。
粗化処理層は、基材層を陰極とした電気めっき法により、金属粒子を基材層上に析出(電着)して形成されるのが好ましい。この場合、金属粒子のサイズ、金属粒子の数等の電着量は、主に電流密度及び電着時間の調整によって制御できる。
電気めっきの条件は、本積層体における電気めっきの条件と同じ条件を採用できる。
なお、金属箔層の表面に対して、ドライエッチング、ウェットエッチング等の粗化処理を施して、その表面の十点平均粗さを上記範囲に調整してもよい。
また、金属箔層は、各種特性を向上させる観点から、耐熱処理層、防錆処理層及びクロメート処理層のうちの少なくとも1つの層を備えてもよい。金属箔層が積層構成である場合、これらの層は、粗化処理層の基材層と反対側の面、又は粗化処理層と金属箔との間に設けられる。なお、耐熱処理層、防錆処理層又はクロメート処理層の形成には、公知の方法を採用できる。また、耐熱処理層、防錆処理層又はクロメート処理層が金属箔層の最外層を構成する場合、その表面が金属箔層の表面を構成する。
金属箔層の厚さは、本積層体の金属箔層の厚さと同じ条件を採用できる。
また、金属箔層は、各種特性を向上させる観点から、耐熱処理層、防錆処理層及びクロメート処理層のうちの少なくとも1つの層を備えてもよい。金属箔層が積層構成である場合、これらの層は、粗化処理層の基材層と反対側の面、又は粗化処理層と金属箔との間に設けられる。なお、耐熱処理層、防錆処理層又はクロメート処理層の形成には、公知の方法を採用できる。また、耐熱処理層、防錆処理層又はクロメート処理層が金属箔層の最外層を構成する場合、その表面が金属箔層の表面を構成する。
金属箔層の厚さは、本積層体の金属箔層の厚さと同じ条件を採用できる。
本複合体の製造方法におけるF層の態様は、その好適な態様、及びその形成法を含めて、本積層体におけるそれと同様である。
本複合体の製造方法における金属箔層の除去は、ウェットエッチングにより行うのが好ましい。ウェットエッチングによれば、F層の接触面に転写された微小な凹凸形状にダメージを与えるのを防止しつつ、金属箔層の不要な部分を正確かつ充分に除去できる。
また、ウェットエッチングは、酸溶液を用いて行うのが好ましい。Fポリマーが上記酸素含有極性基として加水分解性の酸無水物残基を有する場合、酸溶液により酸素含有極性基が活性化するので、F層のプリプレグ層との接着力がさらに高まりやすい。ここで、酸素含有極性基の活性化の一例としては、酸無水物基の1,2-ジカルボン酸基への変換が挙げられる。
酸溶液には、塩酸、希硝酸又はフッ酸等の無機酸水溶液を使用できる。
また、ウェットエッチングは、酸溶液を用いて行うのが好ましい。Fポリマーが上記酸素含有極性基として加水分解性の酸無水物残基を有する場合、酸溶液により酸素含有極性基が活性化するので、F層のプリプレグ層との接着力がさらに高まりやすい。ここで、酸素含有極性基の活性化の一例としては、酸無水物基の1,2-ジカルボン酸基への変換が挙げられる。
酸溶液には、塩酸、希硝酸又はフッ酸等の無機酸水溶液を使用できる。
プリプレグは、強化繊維(ガラス繊維、炭素繊維等)の基材(トウ、織布等)にマトリックス樹脂を含浸させたシート状の基板である。マトリックス樹脂は、熱可塑性樹脂であってもよく、熱硬化性樹脂であってもよい。つまり、プリプレグ層は、プリプレグから形成される層である。プリプレグ層は、マトリックス樹脂が硬化性であればマトリックス樹脂の硬化物を含む層であり、マトリックス樹脂が熱可塑性であればマトリックス樹脂の溶融固化物を含む層である。
熱硬化性樹脂としては、上述した分散液の説明で挙げた樹脂が挙げられ、エポキシ樹脂、ポリフェニレンオキサイド、ポリフェニレンエーテル又はポリブタジエンが好ましい。ポリフェニレンエーテルは、変性ポリフェニレンエーテルが好ましく、ビニル基を有するポリフェニレンエーテルがより好ましい。
熱可塑性樹脂としては、上述した分散液の説明で挙げた樹脂が挙げられる。
マトリックス樹脂は、1種を単独で用いてもよく、2種以上を併用してもよい。
熱硬化性樹脂としては、上述した分散液の説明で挙げた樹脂が挙げられ、エポキシ樹脂、ポリフェニレンオキサイド、ポリフェニレンエーテル又はポリブタジエンが好ましい。ポリフェニレンエーテルは、変性ポリフェニレンエーテルが好ましく、ビニル基を有するポリフェニレンエーテルがより好ましい。
熱可塑性樹脂としては、上述した分散液の説明で挙げた樹脂が挙げられる。
マトリックス樹脂は、1種を単独で用いてもよく、2種以上を併用してもよい。
プリプレグのマトリックス樹脂としては、加工性の点から、エポキシ樹脂、ポリフェニレンオキサイド、ポリフェニレンエーテル又はポリブタジエンが好ましい。
また、マトリックス樹脂が熱硬化性樹脂である場合、プリプレグには硬化剤が含まれるのが好ましく、1分子中に硬化性基(イソシアネート基、ブロックイソシアネート基等)を3つ以上有する硬化剤を含む硬化剤がより好ましい。
マトリックス樹脂として、フッ素原子を有する樹脂を用いてもよい。かかる樹脂としては、Fポリマー、フッ素原子を有するポリイミド、フッ素原子を有するエポキシ樹脂が挙げられる。
マトリックス樹脂の好適な態様としては、フッ素原子を有さないマトリックス樹脂のみからなる態様、フッ素原子を有さないマトリックス樹脂とフッ素原子を有するマトリックス樹脂とからなる態様が挙げられる。
また、マトリックス樹脂が熱硬化性樹脂である場合、プリプレグには硬化剤が含まれるのが好ましく、1分子中に硬化性基(イソシアネート基、ブロックイソシアネート基等)を3つ以上有する硬化剤を含む硬化剤がより好ましい。
マトリックス樹脂として、フッ素原子を有する樹脂を用いてもよい。かかる樹脂としては、Fポリマー、フッ素原子を有するポリイミド、フッ素原子を有するエポキシ樹脂が挙げられる。
マトリックス樹脂の好適な態様としては、フッ素原子を有さないマトリックス樹脂のみからなる態様、フッ素原子を有さないマトリックス樹脂とフッ素原子を有するマトリックス樹脂とからなる態様が挙げられる。
強化繊維シートとしては、複数の強化繊維からなる強化繊維束、該強化繊維束を織成したクロス、複数の強化繊維が一方向に引き揃えられた一方向性強化繊維束、該一方向性強化繊維束から構成された一方向性クロス又はこれらを組み合わせ、複数の強化繊維束の積層物が挙げられる。
強化繊維としては、長さが10mm以上の連続した長繊維が好ましい。強化繊維は、強化繊維シートの長さ方向の全長または幅方向の全幅にわたり連続している必要はなく、途中で分断されていてもよい。強化繊維は、シランカップリング剤処理等の表面処理が施されていてもよい。
強化繊維としては、長さが10mm以上の連続した長繊維が好ましい。強化繊維は、強化繊維シートの長さ方向の全長または幅方向の全幅にわたり連続している必要はなく、途中で分断されていてもよい。強化繊維は、シランカップリング剤処理等の表面処理が施されていてもよい。
強化繊維としては、無機繊維、金属繊維、有機繊維等が挙げられる。
無機繊維としては、炭素繊維、黒鉛繊維、ガラス繊維、シリコンカーバイト繊維、シリコンナイトライド繊維、アルミナ繊維、炭化珪素繊維、ボロン繊維等が挙げられる。
金属繊維としては、アルミニウム繊維、黄銅繊維、ステンレス繊維等が挙げられる。
有機繊維としては、芳香族ポリアミド繊維、ポリアラミド繊維、ポリパラフェニレンベンズオキサゾール(PBO)繊維、ポリフェニレンスルフィド繊維、ポリエステル繊維、アクリル繊維、ナイロン繊維、ポリエチレン繊維等が挙げられる。
強化繊維は、1種を単独で用いてもよく、2種以上を併用してもよい。
プリント基板材料用途における、強化繊維は、ガラス繊維が好ましい。
無機繊維としては、炭素繊維、黒鉛繊維、ガラス繊維、シリコンカーバイト繊維、シリコンナイトライド繊維、アルミナ繊維、炭化珪素繊維、ボロン繊維等が挙げられる。
金属繊維としては、アルミニウム繊維、黄銅繊維、ステンレス繊維等が挙げられる。
有機繊維としては、芳香族ポリアミド繊維、ポリアラミド繊維、ポリパラフェニレンベンズオキサゾール(PBO)繊維、ポリフェニレンスルフィド繊維、ポリエステル繊維、アクリル繊維、ナイロン繊維、ポリエチレン繊維等が挙げられる。
強化繊維は、1種を単独で用いてもよく、2種以上を併用してもよい。
プリント基板材料用途における、強化繊維は、ガラス繊維が好ましい。
F層にプリプレグを接着する方法は、上記積層体の少なくとも一部が露出したF層の接触面にプリプレグを接触させて、熱圧着する方法が好ましい。
熱圧着における温度は、Fポリマーの溶融温度以下が好ましく、120~300℃がより好ましく、160~220℃がさらに好ましい。この範囲において、プリプレグの熱劣化を抑制しつつ、ポリマー層とプリプレグ層とを強固に接着できる。
熱圧着における圧着圧力は、0.2MPa以上が好ましい。また、圧力は、10MPa以下が好ましく、4MPa以下がより好ましい。この範囲において、プリプレグの破損を抑制しつつ、F層とプリプレグ層とをより強固に接着できる。
さらに、かかる熱温度又は圧着圧力にて、F層の接触面にプリプレグを熱圧着させた場合には、アンカー効果によりF層に入り込んだプリプレグ層と、Fポリマーとがより相溶一体化して、接着力がより向上しやすい。
熱圧着における温度は、Fポリマーの溶融温度以下が好ましく、120~300℃がより好ましく、160~220℃がさらに好ましい。この範囲において、プリプレグの熱劣化を抑制しつつ、ポリマー層とプリプレグ層とを強固に接着できる。
熱圧着における圧着圧力は、0.2MPa以上が好ましい。また、圧力は、10MPa以下が好ましく、4MPa以下がより好ましい。この範囲において、プリプレグの破損を抑制しつつ、F層とプリプレグ層とをより強固に接着できる。
さらに、かかる熱温度又は圧着圧力にて、F層の接触面にプリプレグを熱圧着させた場合には、アンカー効果によりF層に入り込んだプリプレグ層と、Fポリマーとがより相溶一体化して、接着力がより向上しやすい。
熱圧着は、減圧雰囲気下で行うことが好ましく、20kPa以下の真空度で行うのがより好ましい。この範囲において、F層とプリプレグ層との界面への気泡混入が抑制でき、本複合体の酸化による劣化を抑制できる。
また、熱プレス時は上記真空度に到達した後に昇温することが好ましい。このようにすれば、F層が軟化する前の状態、すなわち一定程度の流動性、密着性が発現する前の状態にて圧着されるので、気泡の発生を防止できる。
また、熱プレス時は上記真空度に到達した後に昇温することが好ましい。このようにすれば、F層が軟化する前の状態、すなわち一定程度の流動性、密着性が発現する前の状態にて圧着されるので、気泡の発生を防止できる。
本複合体の製造方法によれば、金属箔層の粗さが転写された、接着力の強いF層にプリプレグ層が積層されるため、露出したF層(接触面)の表面を親水化処理することなく、F層をそのままプリプレグ層と接着できる。親水化処理とは、露出したF層の表面に対する水の接触角を下げる処理であり、具体的には、プラズマ処理、電離線処理又はシランカップリング剤による処理が挙げられる。
本複合体において、F層のプリプレグ層に対する剥離強度は、10N/cm以上が好ましく、15N/cm以上がより好ましい。なお、剥離強度の上限は、通常、20N/cmである。
本複合体の反り率は、25%以下が好ましく、7%以下がより好ましい。この場合、本複合体(プリント配線板)の伝送特性が優れる。
本複合体の寸法変化率は、±1%以下が好ましく、±0.2%以下がより好ましい。この場合、本複合体を多層化しやすい。
本複合体において、F層のプリプレグ層に対する剥離強度は、10N/cm以上が好ましく、15N/cm以上がより好ましい。なお、剥離強度の上限は、通常、20N/cmである。
本複合体の反り率は、25%以下が好ましく、7%以下がより好ましい。この場合、本複合体(プリント配線板)の伝送特性が優れる。
本複合体の寸法変化率は、±1%以下が好ましく、±0.2%以下がより好ましい。この場合、本複合体を多層化しやすい。
本複合体の製造方法において、上記積層体の前記金属箔層の一部を除去し、金属箔層から金属回路層(回路パターン)を形成した加工積層体は、はんだリフロー耐性に優れたプリント回路基板として有用である。
例えば、かかるプリント回路基板の多層構造を有し、最外層にF層を有する、多層プリント回路基板は、耐熱性に優れており、具体的には、288℃においても、プリプレグ層の界面での膨れや、金属回路層の界面での剥離が発生しにくい。特に、F層が所定の厚さ(1~15μm、特に3~9μm)にある場合、かかる傾向が顕著になりやすい。
また、かかるプリント回路基板の多層構造を有し、最外層にプリプレグ層を有する、多層プリント回路基板も、耐熱性に優れており、具体的には、300℃においても、プリプレグ層の界面での膨れや、金属回路層の界面での剥離が発生しにくい。特に、F層が所定の厚さ(1~15μm、特に3~9μm)にある場合、かかる傾向が顕著になりやすい。
例えば、かかるプリント回路基板の多層構造を有し、最外層にF層を有する、多層プリント回路基板は、耐熱性に優れており、具体的には、288℃においても、プリプレグ層の界面での膨れや、金属回路層の界面での剥離が発生しにくい。特に、F層が所定の厚さ(1~15μm、特に3~9μm)にある場合、かかる傾向が顕著になりやすい。
また、かかるプリント回路基板の多層構造を有し、最外層にプリプレグ層を有する、多層プリント回路基板も、耐熱性に優れており、具体的には、300℃においても、プリプレグ層の界面での膨れや、金属回路層の界面での剥離が発生しにくい。特に、F層が所定の厚さ(1~15μm、特に3~9μm)にある場合、かかる傾向が顕著になりやすい。
また、本発明によれば、十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に積層されたF層とを有する積層体(F層付金属箔)の前記金属箔の少なくとも一部を除去し、露出したF層にソルダーレジストを塗布し、硬化させてソルダーマスク層を形成し、少なくともF層とソルダーマスク層とが積層された積層体の製造方法が提供される。
この製造方法における、金属箔(金属箔層)、Fポリマー、F層、積層体、及び積層体の金属箔層の少なくとも一部を除去する態様は、好適な範囲も含めて、本複合体の製造方法のそれらと同様である。
この製造方法における、金属箔(金属箔層)、Fポリマー、F層、積層体、及び積層体の金属箔層の少なくとも一部を除去する態様は、好適な範囲も含めて、本複合体の製造方法のそれらと同様である。
ソルダーレジストは、公知のソルダーレジストを使用できる。また、ソルダーレジストの塗布と硬化は、使用するソルダーレジストの種類に応じて、適宜、決定すればよい。
この製造方法において、露出したF層は、その表面を酸溶液で処理し、そのまま直接、ソルダーレジストを塗布して、硬化させるのが好ましい。この場合、ソルダーマスク層の形成において、酸処理後に表面処理(バフ研磨)をする場合に比較して、より密着性に優れたソルダーマスク層を形成しやすい。
この製造方法において、露出したF層は、その表面を酸溶液で処理し、そのまま直接、ソルダーレジストを塗布して、硬化させるのが好ましい。この場合、ソルダーマスク層の形成において、酸処理後に表面処理(バフ研磨)をする場合に比較して、より密着性に優れたソルダーマスク層を形成しやすい。
また、本発明のポリマーフィルムの製造方法では、上記積層体(F層付金属箔)の金属箔層の全てを除去し、残存する単体のF層をポリマーフィルムとして使用できる。
かかるポリマーフィルムは、2つの基材を接着するための接着層、層間絶縁膜、ソルダーレジスト層、カバーレイフィルム等として使用可能である。
かかるポリマーフィルムは、2つの基材を接着するための接着層、層間絶縁膜、ソルダーレジスト層、カバーレイフィルム等として使用可能である。
以上、本発明の積層体及びその製造方法、複合積層体の製造方法、並びにポリマーフィルムの製造方法について説明したが、本発明は、上述した実施形態の構成に限定されない。
例えば、本発明の積層体は、上記実施形態に構成において、他の任意の構成を追加してもよいし、同様の機能を発揮する任意の構成と置換されていてよい。
また、本発明の積層体の製造方法、複合積層体の製造方法、及びポリマーフィルムの製造方法は、それぞれ、上述した実施形態に構成において、他の任意の工程を追加してもよいし、同様の機能を発揮する任意の工程と置換されてもよい。
例えば、本発明の積層体は、上記実施形態に構成において、他の任意の構成を追加してもよいし、同様の機能を発揮する任意の構成と置換されていてよい。
また、本発明の積層体の製造方法、複合積層体の製造方法、及びポリマーフィルムの製造方法は、それぞれ、上述した実施形態に構成において、他の任意の工程を追加してもよいし、同様の機能を発揮する任意の工程と置換されてもよい。
以下、実施例を挙げて本発明を具体的に説明するが、本発明はこれらに限定されない。
1.各成分及び各部材の準備
[Fポリマー]
Fポリマー1:TFEに基づく単位、NAHに基づく単位及びPPVEに基づく単位を、この順に98.0モル%、0.1モル%、1.9モル%含むコポリマー(溶融温度:300℃、380℃の溶融粘度:3×10⁵Pa・s)
Fポリマー2:TFEに基づく単位及びPPVEに基づく単位を、この順に98.0モル%、2.0モル%含む、酸素含有極性基を有さないコポリマー(溶融温度:305℃、380℃の溶融粘度:3×10⁵Pa・s)
Fポリマー3:TFEに基づく単位及びPPVEに基づく単位を、この順に97.5モル%、2.5モル%含む、官能基を有さないコポリマー(溶融温度:305℃、380℃の溶融粘度:3×10⁵Pa・s)
1.各成分及び各部材の準備
[Fポリマー]
Fポリマー1:TFEに基づく単位、NAHに基づく単位及びPPVEに基づく単位を、この順に98.0モル%、0.1モル%、1.9モル%含むコポリマー(溶融温度:300℃、380℃の溶融粘度:3×10⁵Pa・s)
Fポリマー2:TFEに基づく単位及びPPVEに基づく単位を、この順に98.0モル%、2.0モル%含む、酸素含有極性基を有さないコポリマー(溶融温度:305℃、380℃の溶融粘度:3×10⁵Pa・s)
Fポリマー3:TFEに基づく単位及びPPVEに基づく単位を、この順に97.5モル%、2.5モル%含む、官能基を有さないコポリマー(溶融温度:305℃、380℃の溶融粘度:3×10⁵Pa・s)
[パウダー]
パウダー1:Fポリマー1からなるパウダー(D50:2.6μm、D90:7.1μm)
パウダー2:Fポリマー2からなるパウダー(D50:3.5μm、D90:9.2μm)
パウダー3:Fポリマー2からなるパウダー(D50:1.8μm、D90:4.9μm)
パウダー4:Fポリマー1からなるパウダー(D50:1.8μm、D90:5.2μm)
パウダー5:Fポリマー3からなるパウダー(D50:1.9μm、D90:5.5μm)
なお、D50及びD90は、レーザー回折・散乱式粒度分布測定装置(堀場製作所社製、LA-920測定器)を用い、パウダーを水中に分散させて測定した。
パウダー1:Fポリマー1からなるパウダー(D50:2.6μm、D90:7.1μm)
パウダー2:Fポリマー2からなるパウダー(D50:3.5μm、D90:9.2μm)
パウダー3:Fポリマー2からなるパウダー(D50:1.8μm、D90:4.9μm)
パウダー4:Fポリマー1からなるパウダー(D50:1.8μm、D90:5.2μm)
パウダー5:Fポリマー3からなるパウダー(D50:1.9μm、D90:5.5μm)
なお、D50及びD90は、レーザー回折・散乱式粒度分布測定装置(堀場製作所社製、LA-920測定器)を用い、パウダーを水中に分散させて測定した。
[フッ素系分散剤]
FP1:ノニオン性のフルオロポリオールである、CH2=CHCOO(CH2)4OCF(CF3)(C(CF(CF3)2)(=C(CF3)2)とCH2=CHCOO(CH2)4(OCH2CH2)10OHのコポリマー
[シート]
シート1:Fポリマー1からなるシート(厚さ:10μm)
シート2:Fポリマー3からなるシート(厚さ:10μm)
[プリプレグ]
プリプレグ1:ポリフェニレンエーテル系樹脂とガラス繊維とシリカフィラーとを含む熱硬化性の樹脂組成物
FP1:ノニオン性のフルオロポリオールである、CH2=CHCOO(CH2)4OCF(CF3)(C(CF(CF3)2)(=C(CF3)2)とCH2=CHCOO(CH2)4(OCH2CH2)10OHのコポリマー
[シート]
シート1:Fポリマー1からなるシート(厚さ:10μm)
シート2:Fポリマー3からなるシート(厚さ:10μm)
[プリプレグ]
プリプレグ1:ポリフェニレンエーテル系樹脂とガラス繊維とシリカフィラーとを含む熱硬化性の樹脂組成物
2.分散液の調製
(分散液1)
47質量部のN-メチル-2-ピロリドン(NMP)と、2.5質量部のFP1と、50質量部のパウダー1とをポットに投入した後、ポット内にジルコニアボールを投入した。その後、150rpmにて1時間、ポットをころがし、パウダー1をNMPに分散させて分散液1を調製した。
(分散液2)
パウダー1をパウダー2に変更した以外は、分散液1と同様にして、分散液2を調製した。
(分散液1)
47質量部のN-メチル-2-ピロリドン(NMP)と、2.5質量部のFP1と、50質量部のパウダー1とをポットに投入した後、ポット内にジルコニアボールを投入した。その後、150rpmにて1時間、ポットをころがし、パウダー1をNMPに分散させて分散液1を調製した。
(分散液2)
パウダー1をパウダー2に変更した以外は、分散液1と同様にして、分散液2を調製した。
(分散液3)
パウダー1をパウダー3に変更した以外は、分散液1と同様にして、分散液3を調製した。
(分散液4)
パウダー1をパウダー4に、FP1の量を3質量部に変更した以外は、分散液1と同様にして、分散液4を調製した。
(分散液5)
パウダー1をパウダー5に、FP1の量を3質量部に変更した以外は、分散液1と同様にして、分散液5を調製した。
パウダー1をパウダー3に変更した以外は、分散液1と同様にして、分散液3を調製した。
(分散液4)
パウダー1をパウダー4に、FP1の量を3質量部に変更した以外は、分散液1と同様にして、分散液4を調製した。
(分散液5)
パウダー1をパウダー5に、FP1の量を3質量部に変更した以外は、分散液1と同様にして、分散液5を調製した。
3.金属箔の作製
(金属箔1)
厚さ12μmの圧延銅箔(基材層)を陰極として、以下の条件で電気めっきを行って、圧延銅箔の表面に粗化処理層を形成した。これにより、金属箔1を作製した。
その後、粗化処理層の表面に、耐熱処理層及びクロメート層を順次形成した。
なお、金属箔1の厚さは、15μmであり、表面の十点平均粗さは、0.6μmであった。
<1次粒子めっき(1)>
液組成 :硫酸銅五水和物11g/L、硫酸52g/L
液温 :22℃
電流密度:40A/dm2
電着時間:1秒
<1次粒子めっき(2)>
液組成 :硫酸銅五水和物19g/L、硫酸101g/L
液温 :42℃
電流密度:4A/dm2
電着時間:3秒
<2次粒子めっき>
液組成 :硫酸銅五水和物15g/L、硫酸ニッケル六水和物10g/L
、硫酸コバルト七水和物7g/L
液温 :37℃
電流密度:30A/dm2
電着時間:1秒
(金属箔1)
厚さ12μmの圧延銅箔(基材層)を陰極として、以下の条件で電気めっきを行って、圧延銅箔の表面に粗化処理層を形成した。これにより、金属箔1を作製した。
その後、粗化処理層の表面に、耐熱処理層及びクロメート層を順次形成した。
なお、金属箔1の厚さは、15μmであり、表面の十点平均粗さは、0.6μmであった。
<1次粒子めっき(1)>
液組成 :硫酸銅五水和物11g/L、硫酸52g/L
液温 :22℃
電流密度:40A/dm2
電着時間:1秒
<1次粒子めっき(2)>
液組成 :硫酸銅五水和物19g/L、硫酸101g/L
液温 :42℃
電流密度:4A/dm2
電着時間:3秒
<2次粒子めっき>
液組成 :硫酸銅五水和物15g/L、硫酸ニッケル六水和物10g/L
、硫酸コバルト七水和物7g/L
液温 :37℃
電流密度:30A/dm2
電着時間:1秒
(金属箔2)
金属箔1の表面に、シランカップリング剤(信越化学工業株式会社製、「KBMシリーズ」)を1体積%で含む溶液を用い、下記の条件で表面処理して、金属箔2を作製した。
なお、金属箔2の厚さは、15μmであり、表面の十点平均粗さは、0.6μmであった。
<処理条件>
溶液の温度:20℃
溶液のpH:4.5
処理時間 :3秒
塗布回数 :1回
乾燥温度 :110℃
乾燥時間 :30秒
金属箔1の表面に、シランカップリング剤(信越化学工業株式会社製、「KBMシリーズ」)を1体積%で含む溶液を用い、下記の条件で表面処理して、金属箔2を作製した。
なお、金属箔2の厚さは、15μmであり、表面の十点平均粗さは、0.6μmであった。
<処理条件>
溶液の温度:20℃
溶液のpH:4.5
処理時間 :3秒
塗布回数 :1回
乾燥温度 :110℃
乾燥時間 :30秒
(金属箔3)
陽極として白金属酸化物で被覆したチタンを使用し、陰極として十点平均粗さ(Rzjis)が0.75μmかつ厚さが12μmの電解銅箔を使用し、以下の条件で電気めっきを行って、電解銅箔の表面に粗化処理層を形成し、金属箔3を作製した。
<めっき条件>
液組成 :硫酸銅五水和物15g/L、硫酸コバルト七水和物8.5g/
L、硫酸ニッケル六水和物1.7g/L
pH :2.5
液温 :38℃
電流密度:45A/dm2
電着時間:1秒
なお、金属箔3の表面の十点平均粗さは、1.0μmであった。
また、金属箔3(粗化処理層)の表面を、測定径をφ30mmとして、蛍光X線分析装置(株式会社リガク社製、ZSX PrimusII)を用いて分析した。その結果、ニッケル原子の割合(ニッケル原子の質量/全原子の質量)は、0.06質量%であった。
陽極として白金属酸化物で被覆したチタンを使用し、陰極として十点平均粗さ(Rzjis)が0.75μmかつ厚さが12μmの電解銅箔を使用し、以下の条件で電気めっきを行って、電解銅箔の表面に粗化処理層を形成し、金属箔3を作製した。
<めっき条件>
液組成 :硫酸銅五水和物15g/L、硫酸コバルト七水和物8.5g/
L、硫酸ニッケル六水和物1.7g/L
pH :2.5
液温 :38℃
電流密度:45A/dm2
電着時間:1秒
なお、金属箔3の表面の十点平均粗さは、1.0μmであった。
また、金属箔3(粗化処理層)の表面を、測定径をφ30mmとして、蛍光X線分析装置(株式会社リガク社製、ZSX PrimusII)を用いて分析した。その結果、ニッケル原子の割合(ニッケル原子の質量/全原子の質量)は、0.06質量%であった。
(金属箔4)
以下に示す液組成に変更した以外は、金属箔3と同様にして、金属箔4を作製した。
液組成:硫酸銅五水和物15g/L、硫酸コバルト七水和物8.5g/L
なお、金属箔4の表面の十点平均粗さは、1.0μmであった。また、上記と同様にして測定された金属箔4(粗化処理層)の表面に存在するニッケル原子の割合は、0.00質量%であった。
(金属箔5)
以下に示す液組成に変更した以外は、金属箔3と同様にして、金属箔5を作製した。
液組成:硫酸銅五水和物15g/L、硫酸コバルト七水和物8.5g/L
、硫酸ニッケル六水和物8.6g/L
なお、金属箔5の表面の十点平均粗さは、1.0μmであった。また、上記と同様にして測定された金属箔5(粗化処理層)の表面に存在するニッケル原子の割合は、0.30質量%であった。
以下に示す液組成に変更した以外は、金属箔3と同様にして、金属箔4を作製した。
液組成:硫酸銅五水和物15g/L、硫酸コバルト七水和物8.5g/L
なお、金属箔4の表面の十点平均粗さは、1.0μmであった。また、上記と同様にして測定された金属箔4(粗化処理層)の表面に存在するニッケル原子の割合は、0.00質量%であった。
(金属箔5)
以下に示す液組成に変更した以外は、金属箔3と同様にして、金属箔5を作製した。
液組成:硫酸銅五水和物15g/L、硫酸コバルト七水和物8.5g/L
、硫酸ニッケル六水和物8.6g/L
なお、金属箔5の表面の十点平均粗さは、1.0μmであった。また、上記と同様にして測定された金属箔5(粗化処理層)の表面に存在するニッケル原子の割合は、0.30質量%であった。
(金属箔6)
電解銅箔に電気めっき処理して粗化処理層を形成した後、粗化処理層上に耐熱処理層及びクロメート層を順次形成して金属箔6を製造した。なお、金属箔6の表面の十点平均粗さは0.2μmであり、厚さは12μmであった。
(金属箔7)
金属箔6と同様にして、金属箔7を製造した。なお、金属箔7の表面の十点平均粗さは1.2μmであり、厚さは18μmであった。
(金属箔8)
金属箔6と同様にして、金属箔8を製造した。なお、金属箔8の表面の十点平均粗さは7.7μmであり、厚さは18μmであった。
電解銅箔に電気めっき処理して粗化処理層を形成した後、粗化処理層上に耐熱処理層及びクロメート層を順次形成して金属箔6を製造した。なお、金属箔6の表面の十点平均粗さは0.2μmであり、厚さは12μmであった。
(金属箔7)
金属箔6と同様にして、金属箔7を製造した。なお、金属箔7の表面の十点平均粗さは1.2μmであり、厚さは18μmであった。
(金属箔8)
金属箔6と同様にして、金属箔8を製造した。なお、金属箔8の表面の十点平均粗さは7.7μmであり、厚さは18μmであった。
4.積層体の製造
(例1)
まず、金属箔1の表面に、分散液1をダイコートによりロールツーロールで塗工して、液状被膜を形成した。次いで、この液状被膜が形成された金属箔1を、120℃にて30分間、乾燥炉に通し、加熱により乾燥させた。その後、窒素オーブン中で、乾燥被膜を380℃にて15分間、加熱した。これにより、金属箔1の表面にF層が形成された積層体1を製造した。
(例1)
まず、金属箔1の表面に、分散液1をダイコートによりロールツーロールで塗工して、液状被膜を形成した。次いで、この液状被膜が形成された金属箔1を、120℃にて30分間、乾燥炉に通し、加熱により乾燥させた。その後、窒素オーブン中で、乾燥被膜を380℃にて15分間、加熱した。これにより、金属箔1の表面にF層が形成された積層体1を製造した。
(例2(比較例))
金属箔1を金属箔2に変更した以外は、例1と同様にして、積層体2を製造した。
(例3(比較例))
分散液1を分散液2に変更した以外は、例1と同様にして、積層体3を製造した。
金属箔1を金属箔2に変更した以外は、例1と同様にして、積層体2を製造した。
(例3(比較例))
分散液1を分散液2に変更した以外は、例1と同様にして、積層体3を製造した。
(例4)
金属箔1を金属箔3に変更した以外は、例1と同様にして、F層の厚さが12μmの積層体4を製造した。
この積層体4の2枚とポリイミドフィルム(厚さ:25μm;宇部興産株式会社製、「ユーピレックス25S」)の1枚とを使用し、ポリイミドフィルムの両面にそれぞれの積層体1のF層を当てて360℃にて加熱積層して、両方の最表面に金属箔層を有する積層体41をさらに製造した。
金属箔1を金属箔3に変更した以外は、例1と同様にして、F層の厚さが12μmの積層体4を製造した。
この積層体4の2枚とポリイミドフィルム(厚さ:25μm;宇部興産株式会社製、「ユーピレックス25S」)の1枚とを使用し、ポリイミドフィルムの両面にそれぞれの積層体1のF層を当てて360℃にて加熱積層して、両方の最表面に金属箔層を有する積層体41をさらに製造した。
(例5(比較例))
金属箔3を金属箔4に変更した以外は、例4と同様にして、F層の厚さが12μmの積層体5と積層体51とを製造した。
(例6(比較例))
金属箔3を金属箔5に変更した以外は、例4と同様にして、F層の厚さが12μmの積層体6と積層体61とを製造した。
(例7(比較例))
分散液1を分散液3に変更した以外は、例4と同様にして、F層の厚さが12μmの積層体7を製造した。
金属箔3を金属箔4に変更した以外は、例4と同様にして、F層の厚さが12μmの積層体5と積層体51とを製造した。
(例6(比較例))
金属箔3を金属箔5に変更した以外は、例4と同様にして、F層の厚さが12μmの積層体6と積層体61とを製造した。
(例7(比較例))
分散液1を分散液3に変更した以外は、例4と同様にして、F層の厚さが12μmの積層体7を製造した。
(例8)
まず、金属箔7の表面に、分散液4をグラビアリバース法によりロールツーロールで塗工して、液状被膜を形成した。次いで、この液状被膜が形成された金属箔7を、100℃、120℃及び140℃の乾燥炉のそれぞれに、計5分間、通し、加熱により乾燥させた。その後、窒素雰囲気下の遠赤外線オーブン中で、乾燥被膜を380℃にて3分間、加熱した。これにより、金属箔層の表面にF層が形成された積層体8を製造した。なお、F層の厚さは5μmであった。
次に、積層体8のF層側を真空プラズマ処理した後、積層体8のF層とプリプレグ1とを積層して、温度200℃、圧力3MPa、時間15分の条件にて熱圧着した。次に、積層体8の金属箔層の全てを酸溶液で除去し、その接触面(露出面)に、そのままプリプレグ1を積層して温度200℃、圧力3MPa、時間15分の条件にて熱圧着した。これにより、露出したF層とプリプレグ層とが積層された複合積層体8を得た。
まず、金属箔7の表面に、分散液4をグラビアリバース法によりロールツーロールで塗工して、液状被膜を形成した。次いで、この液状被膜が形成された金属箔7を、100℃、120℃及び140℃の乾燥炉のそれぞれに、計5分間、通し、加熱により乾燥させた。その後、窒素雰囲気下の遠赤外線オーブン中で、乾燥被膜を380℃にて3分間、加熱した。これにより、金属箔層の表面にF層が形成された積層体8を製造した。なお、F層の厚さは5μmであった。
次に、積層体8のF層側を真空プラズマ処理した後、積層体8のF層とプリプレグ1とを積層して、温度200℃、圧力3MPa、時間15分の条件にて熱圧着した。次に、積層体8の金属箔層の全てを酸溶液で除去し、その接触面(露出面)に、そのままプリプレグ1を積層して温度200℃、圧力3MPa、時間15分の条件にて熱圧着した。これにより、露出したF層とプリプレグ層とが積層された複合積層体8を得た。
(例9)
金属箔7を金属箔6に、分散液4を分散液5に変更した以外は、例8と同様にして、複合積層体9を製造した。
(例10)
分散液4を分散液5に変更した以外は、例8と同様にして、複合積層体10を製造した。
(例11(比較例))
金属箔7を金属箔8に変更し、F層の厚さを15μmとした以外は、例10と同様にして、複合積層体11を製造した。
金属箔7を金属箔6に、分散液4を分散液5に変更した以外は、例8と同様にして、複合積層体9を製造した。
(例10)
分散液4を分散液5に変更した以外は、例8と同様にして、複合積層体10を製造した。
(例11(比較例))
金属箔7を金属箔8に変更し、F層の厚さを15μmとした以外は、例10と同様にして、複合積層体11を製造した。
(例12)
まず、金属箔7の表面にシート1を積層し、窒素雰囲気下のオーブン中で380℃にて3分間、熱圧着した。これにより、金属箔層の表面にF層が形成された積層体を製造した。
次に、積層体のF層側を真空プラズマ処理した後、積層体のF層とプリプレグ1とを積層して、温度200℃、圧力3MPa、時間15分の条件にて熱圧着した。次に、積層体の金属箔層の全てを酸溶液で除去し、その接触面(露出面)に、そのままプリプレグ1を積層して温度200℃、圧力3MPa、時間15分の条件にて熱圧着した。これにより、露出したF層とプリプレグ層とが積層された複合積層体12を得た。
(例13)
シート1をシート2に変更した以外は、例12と同様にして、複合積層体13を製造した。
まず、金属箔7の表面にシート1を積層し、窒素雰囲気下のオーブン中で380℃にて3分間、熱圧着した。これにより、金属箔層の表面にF層が形成された積層体を製造した。
次に、積層体のF層側を真空プラズマ処理した後、積層体のF層とプリプレグ1とを積層して、温度200℃、圧力3MPa、時間15分の条件にて熱圧着した。次に、積層体の金属箔層の全てを酸溶液で除去し、その接触面(露出面)に、そのままプリプレグ1を積層して温度200℃、圧力3MPa、時間15分の条件にて熱圧着した。これにより、露出したF層とプリプレグ層とが積層された複合積層体12を得た。
(例13)
シート1をシート2に変更した以外は、例12と同様にして、複合積層体13を製造した。
5.積層体の評価
5-1.積層体の金属箔層とF層との間の剥離強度(その1)
例1~例3の積層体を矩形状(長さ100mm、幅10mm)に切り出して、50個のサンプルを作製した。次に、各サンプルの長さ方向の一端から50mmの位置を固定し、引張り速度50mm/分、長さ方向の片端からサンプルに対して90°で、金属箔層とF層とを剥離させた際にかかる最大荷重(N/cm)を測定した。
結果を、まとめて表1に示す。
5-1.積層体の金属箔層とF層との間の剥離強度(その1)
例1~例3の積層体を矩形状(長さ100mm、幅10mm)に切り出して、50個のサンプルを作製した。次に、各サンプルの長さ方向の一端から50mmの位置を固定し、引張り速度50mm/分、長さ方向の片端からサンプルに対して90°で、金属箔層とF層とを剥離させた際にかかる最大荷重(N/cm)を測定した。
結果を、まとめて表1に示す。

積層体1では、金属箔の表面がシランカップリング剤で処理されていないため、高い剥離強度が得られ、サンプル間の剥離強度のばらつきが小さかった。
これに対して、積層体2では、金属箔の表面がシランカップリング剤で処理されているため、充分な剥離強度が得られないだけでなく、サンプル間の剥離強度のばらつきも大きかった。また、積層体3では、酸素含有極性基を有さないFポリマー2を使用したため、表面がシランカップリング剤で処理されていない金属箔を使用したが、剥離強度が低かった。
これに対して、積層体2では、金属箔の表面がシランカップリング剤で処理されているため、充分な剥離強度が得られないだけでなく、サンプル間の剥離強度のばらつきも大きかった。また、積層体3では、酸素含有極性基を有さないFポリマー2を使用したため、表面がシランカップリング剤で処理されていない金属箔を使用したが、剥離強度が低かった。
5-2.積層体の金属箔層とF層との間の剥離強度(その2)
5-2-1.積層体の金属箔層とF層との間の初期剥離強度
2つの積層体4を、F層同士が接触するように重ね合わせ、340℃にて20分間、真空プレスし、サンプルを得た。このサンプルに対して、IPC-TM650-2.4.9.E MethodAに準拠し、3.2mm幅にエッチングした金属箔層を90°の角度で剥離して、その剥離強度を測定した。積層体5~7のそれぞれについても、積層体4と同様にして作製したサンプルの剥離強度を測定した。
5-2-2.積層体の金属箔層とF層との間の加熱後剥離強度
5-2-1で作製したそれぞれのサンプルを、150℃のオーブンに入れて加熱し、1000時間経過後に、5-2-1と同様の方法で剥離強度を測定した。
また、以下の計算式に従って、保持率(%)を求めた。
保持率(%)=(加熱後の剥離強度)/(初期剥離強度)×100
結果を、まとめて表2に示す。
5-2-1.積層体の金属箔層とF層との間の初期剥離強度
2つの積層体4を、F層同士が接触するように重ね合わせ、340℃にて20分間、真空プレスし、サンプルを得た。このサンプルに対して、IPC-TM650-2.4.9.E MethodAに準拠し、3.2mm幅にエッチングした金属箔層を90°の角度で剥離して、その剥離強度を測定した。積層体5~7のそれぞれについても、積層体4と同様にして作製したサンプルの剥離強度を測定した。
5-2-2.積層体の金属箔層とF層との間の加熱後剥離強度
5-2-1で作製したそれぞれのサンプルを、150℃のオーブンに入れて加熱し、1000時間経過後に、5-2-1と同様の方法で剥離強度を測定した。
また、以下の計算式に従って、保持率(%)を求めた。
保持率(%)=(加熱後の剥離強度)/(初期剥離強度)×100
結果を、まとめて表2に示す。
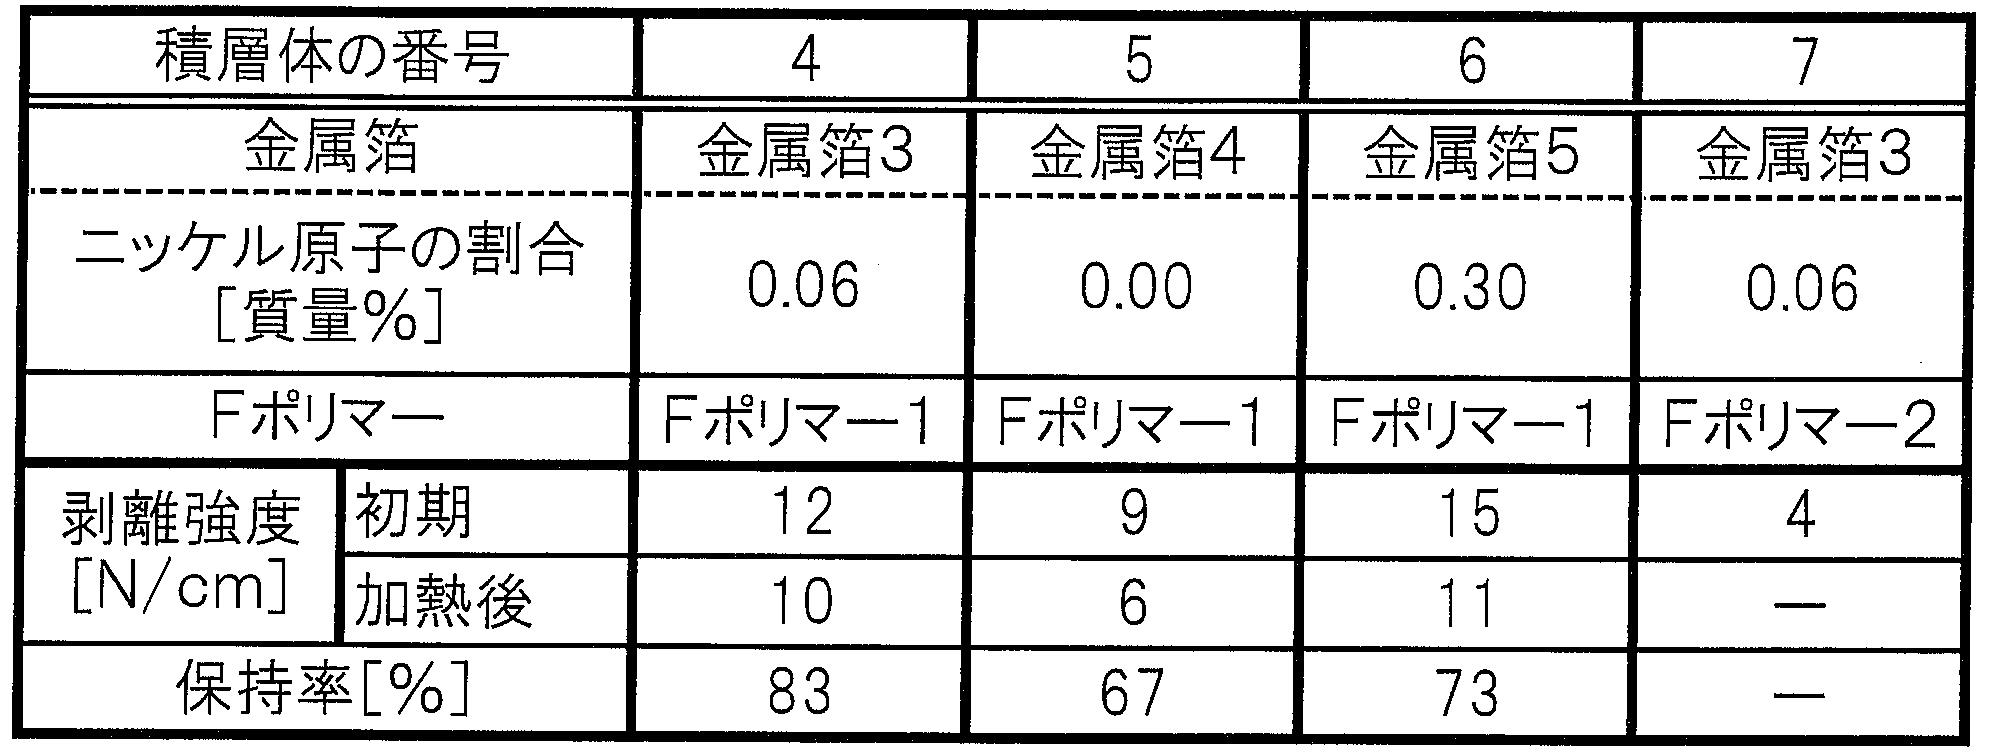
5-3.伝送損失の測定
積層体41を用い、マイクロストリップラインのサンプル回路を形成した。シグナル層の線幅は120μm、線長50mm、裏面はベタのグランド層とした。UTF(Universal Test Fixture)でサンプル回路を挟み込み、ネットワークアナライザを使用して40GHzでの伝送損失を測定した。積層体51及び積層体61のそれぞれについても、積層体41と同様にして、伝送損失を測定した。
結果を、まとめて表3に示す。
積層体41を用い、マイクロストリップラインのサンプル回路を形成した。シグナル層の線幅は120μm、線長50mm、裏面はベタのグランド層とした。UTF(Universal Test Fixture)でサンプル回路を挟み込み、ネットワークアナライザを使用して40GHzでの伝送損失を測定した。積層体51及び積層体61のそれぞれについても、積層体41と同様にして、伝送損失を測定した。
結果を、まとめて表3に示す。
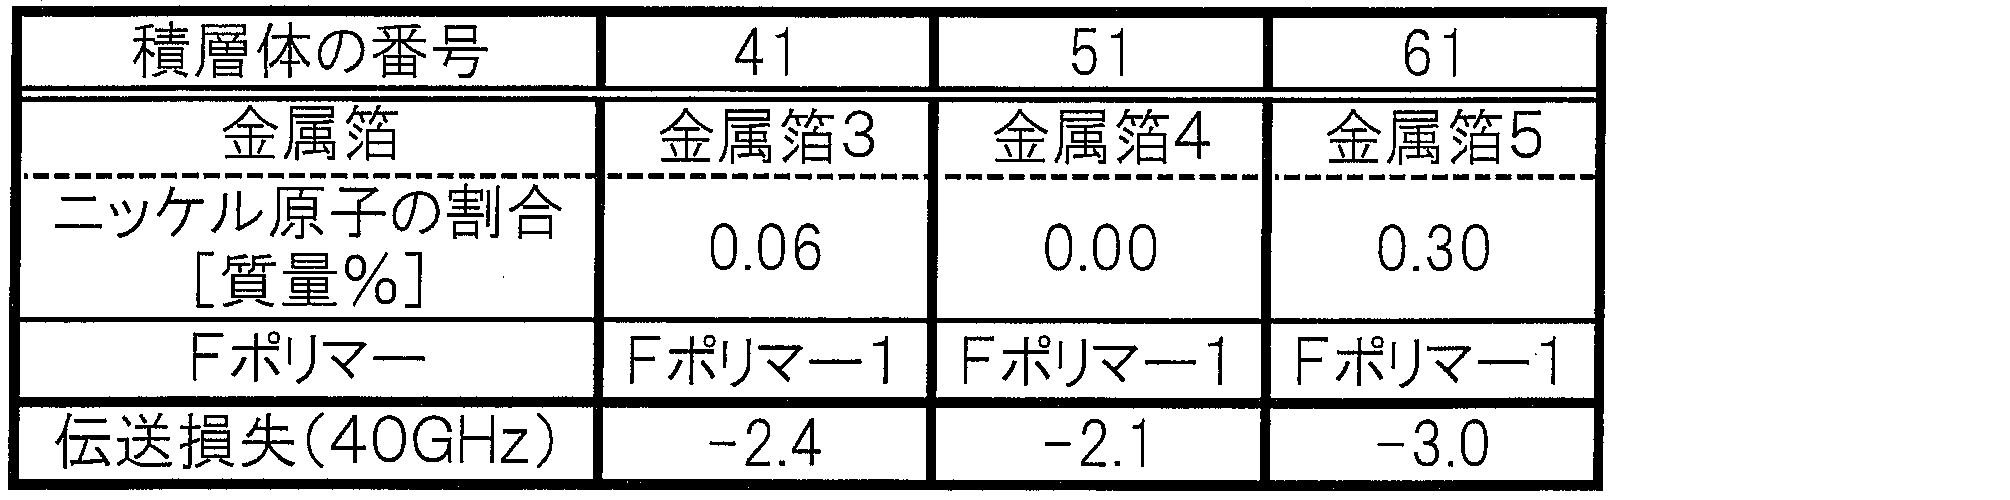
5-4.複合積層体のプリプレグ層とF層と間の剥離強度(その3)
複合積層体8を矩形状(長さ100mm、幅10mm)に切り出して、サンプルを作製した。次に、サンプルの長さ方向の一端から50mmの位置を固定し、引張り速度50mm/分、長さ方向の片端からサンプルに対して90°で、プリプレグ層とF層とを剥離させた際にかかる最大荷重(N/cm)を測定した。複合積層体9~13のそれぞれについても、複合積層体8と同様にして作製したサンプルの剥離強度を測定し、以下の基準に従って評価した。
[評価基準]
◎:15N/cm以上
〇:10N/cm以上15N/cm未満
△: 5N/cm以上10N/cm未満
×: 5N/cm未満
結果を、まとめて表4に示す。
複合積層体8を矩形状(長さ100mm、幅10mm)に切り出して、サンプルを作製した。次に、サンプルの長さ方向の一端から50mmの位置を固定し、引張り速度50mm/分、長さ方向の片端からサンプルに対して90°で、プリプレグ層とF層とを剥離させた際にかかる最大荷重(N/cm)を測定した。複合積層体9~13のそれぞれについても、複合積層体8と同様にして作製したサンプルの剥離強度を測定し、以下の基準に従って評価した。
[評価基準]
◎:15N/cm以上
〇:10N/cm以上15N/cm未満
△: 5N/cm以上10N/cm未満
×: 5N/cm未満
結果を、まとめて表4に示す。
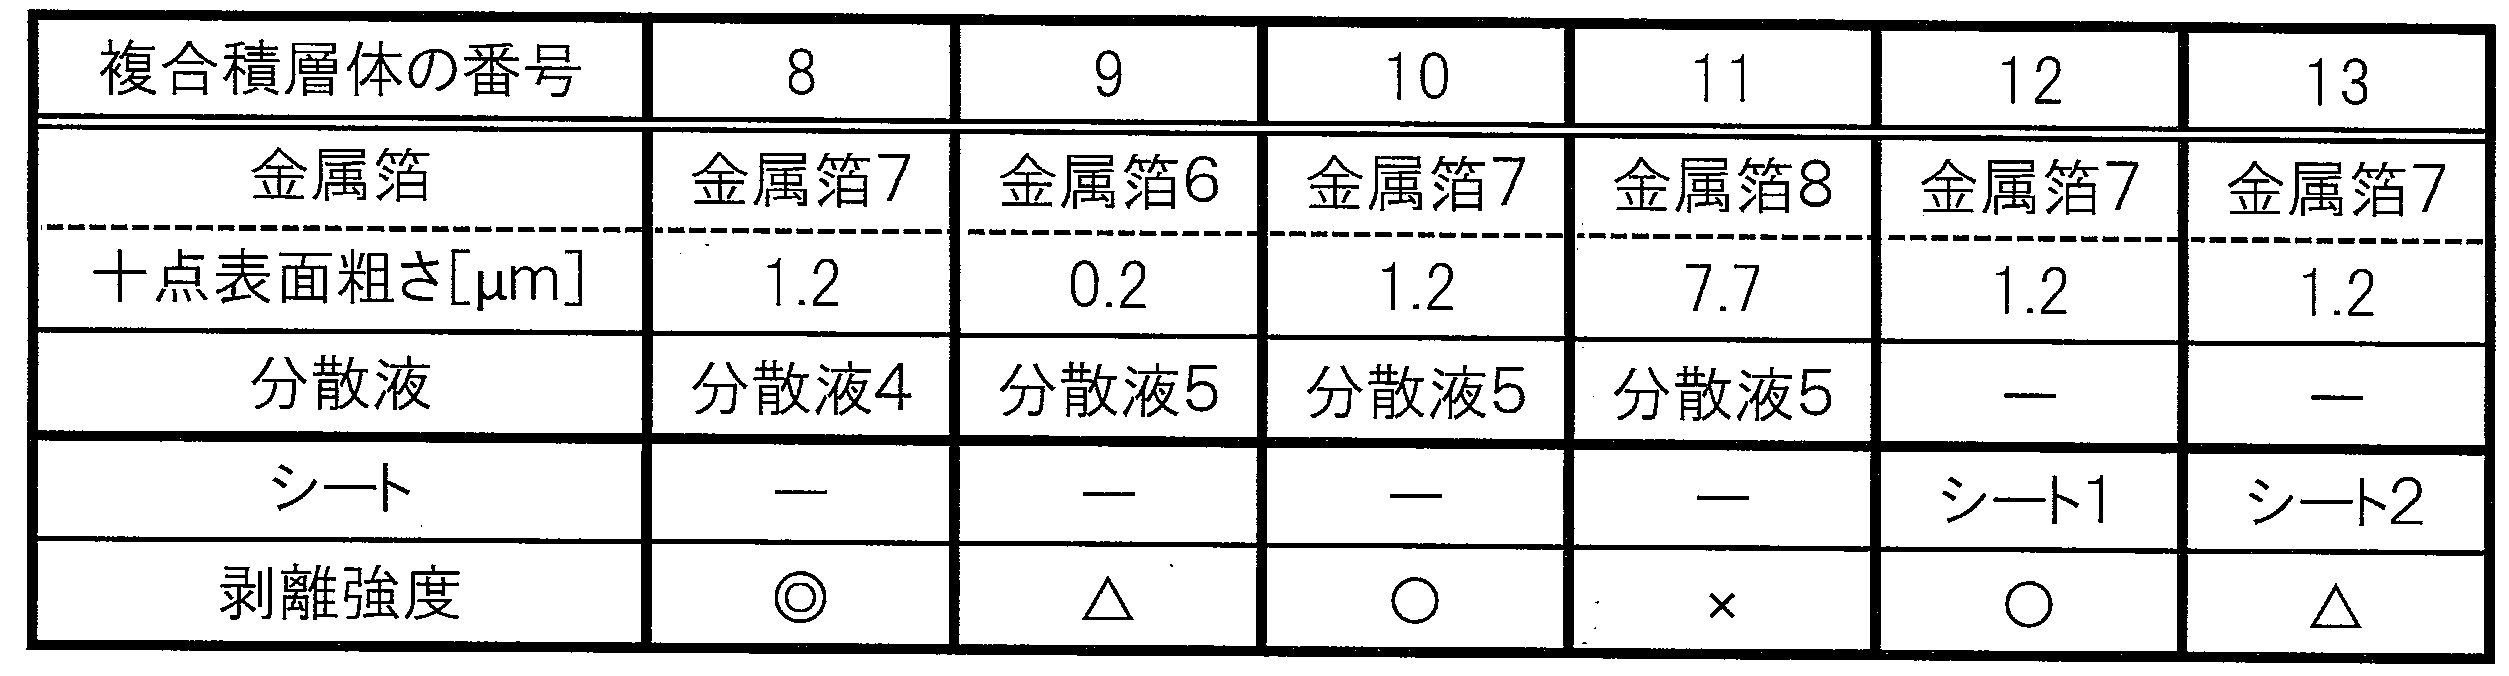
6.ソルダーマスク層を備えた複合積層体の製造
(例14)
積層体8のF層とプリプレグ1とを、例8と同様にして、積層して熱圧着した。次に、金属箔層の全てを酸溶液で除去し、その接触面(露出面)をソフトエッチング剤(四国化成工業社製、「グリブライトGB-4300」)にて処理した。なお、ソフトエッチング剤は、硫酸及び過酸化水素を含む水溶液である。その後、処理済みの露出面に、そのまま(バフ研磨せずに)直接、ソルダーレジスト(太陽インキ社製、「PSR-4000 LD1K」)を厚さ30μmとなるように、スクリーン印刷法にて塗布した。
(例14)
積層体8のF層とプリプレグ1とを、例8と同様にして、積層して熱圧着した。次に、金属箔層の全てを酸溶液で除去し、その接触面(露出面)をソフトエッチング剤(四国化成工業社製、「グリブライトGB-4300」)にて処理した。なお、ソフトエッチング剤は、硫酸及び過酸化水素を含む水溶液である。その後、処理済みの露出面に、そのまま(バフ研磨せずに)直接、ソルダーレジスト(太陽インキ社製、「PSR-4000 LD1K」)を厚さ30μmとなるように、スクリーン印刷法にて塗布した。
次に、ソルダーレジストを80℃にて3分間乾燥し、400mJ/cm2のUV光を露光した後、1質量%の炭酸ナトリウム水溶液に60秒間、浸漬して現像した。その後、ソルダーレジストを150℃にて60分間ポストキュアし、さらに1000mJ/cm2のUV光を露光してソルダーマスク層を形成し、露出したF層とソルダーマスク層とが積層された複合積層体14を得た。
(例15)
金属箔8を使用した以外は、例14と同様にして、複合積層体15を得た。
(例16)
F層の接触面(露出面)をソフトエッチング剤にて処理し、バフ研磨した後、ソルダーレジストを塗布した以外は、例14と同様にして、複合積層体16を得た。
金属箔8を使用した以外は、例14と同様にして、複合積層体15を得た。
(例16)
F層の接触面(露出面)をソフトエッチング剤にて処理し、バフ研磨した後、ソルダーレジストを塗布した以外は、例14と同様にして、複合積層体16を得た。
7.密着性の評価
積層体14~16のそれぞれについて、F層とソルダーレジスト層との密着性を、K5600-5-6:1999(ISO 2409:1992)に規定される100マスのクロスカット試験にて評価した結果、複合積層体14は、カットの縁が完全に滑らかでどの格子の目にも剥がれが生じていなかった。
複合積層体15は、カットの縁に沿って、大幅に剥がれが生じていた。
複合積層体16は、カットの縁に沿って、かつカットの交差点において、一部に剥がれが確認された。
積層体14~16のそれぞれについて、F層とソルダーレジスト層との密着性を、K5600-5-6:1999(ISO 2409:1992)に規定される100マスのクロスカット試験にて評価した結果、複合積層体14は、カットの縁が完全に滑らかでどの格子の目にも剥がれが生じていなかった。
複合積層体15は、カットの縁に沿って、大幅に剥がれが生じていた。
複合積層体16は、カットの縁に沿って、かつカットの交差点において、一部に剥がれが確認された。
本発明の積層体及び本発明により製造される複合積層体は、電気特性及び接着性に優れ、金属箔層に強固に固定されたポリマー層を有するため、アンテナ部品、プリント配線板、パワー半導体の絶縁層、航空機用部品、自動車用部品等に加工して使用できる。
Claims (15)
- 金属箔層と、前記金属箔層の表面に直接接触して設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体であって、前記金属箔層が、前記表面にケイ素原子が存在しない金属箔層、又は前記表面を蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔層である、積層体。
- 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備える、請求項1に記載の積層体。
- 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備え、前記金属粒子は、銅、ニッケル、リン、タングステン、ヒ素、モリブデン、クロム、コバルト、亜鉛又はこれらの1種以上を含む合金で形成されている、請求項1又は2に記載の積層体。
- 前記金属箔層が、基材層と、金属粒子で構成され、前記表面を有する粗化処理層とを備え、前記金属粒子は、針状をなす金属粒子を含む、請求項1~3のいずれか1項に記載の積層体。
- 前記金属箔層の前記表面の十点平均粗さが、0.1μm以上である、請求項1~4のいずれか1項に記載の積層体。
- 前記テトラフルオロエチレン系ポリマーが、ペルフルオロ(アルキルビニルエーテル)に基づく単位に基づく単位を含むテトラフルオロエチレン系ポリマー、又は、数平均分子量が20万以下であるポリテトラフルオロエチレンである、請求項1~5のいずれか1項に記載の積層体。
- 前記テトラフルオロエチレン系ポリマーが、ペルフルオロ(アルキルビニルエーテル)に基づく単位を含み、酸素含有極性基を有するテトラフルオロエチレン系ポリマー、又は、ペルフルオロ(アルキルビニルエーテル)に基づく単位を全単位に対して2.0~5.0モル%含み、酸素含有極性基を有さないテトラフルオロエチレン系ポリマーである、請求項1~6のいずれか1項に記載の積層体。
- 前記ポリマー層の前記金属箔層に対する剥離強度が、10N/cm以上である、請求項1~7のいずれか1項に記載の積層体。
- 金属箔の表面をシランカップリング剤で処理することなく、前記金属箔の前記表面に、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層を直接接触して形成し、前記金属箔で構成される金属箔層の表面に直接接触して設けられた前記ポリマー層を有する積層体を得る、積層体の製造方法。
- 蛍光X線分析したときに検出されるニッケル原子の割合が0.03~0.25質量%である金属箔の表面に、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層を直接接触して形成し、前記金属箔で構成される金属箔層の表面に直接接触して設けられた前記ポリマー層を有する積層体を得る、積層体の製造方法。
- 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層の少なくとも一部を除去し、露出した前記ポリマー層とプリプレグとを接着させ、少なくとも前記ポリマー層とプリプレグ層とが積層された複合積層体を得る、複合積層体の製造方法。
- 前記露出した前記ポリマー層の表面を親水化処理することなく、前記プリプレグと接着させる、請求項11に記載の製造方法。
- 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層の少なくとも一部を除去し、露出した前記ポリマー層にソルダーレジストを塗布し、硬化させてソルダーマスク層を形成し、少なくとも前記ポリマー層とソルダーマスク層とが積層された複合積層体を得る、複合積層体の製造方法。
- 前記露出した前記ポリマー層の表面を酸溶液で処理し、そのまま直接、ソルダーレジストを塗布し、硬化させてソルダーマスク層を形成する、請求項13に記載の製造方法。
- 十点平均粗さが0.1μm以上の表面を有する金属箔層と、前記表面に設けられ、380℃における溶融粘度が1×10²~1×10⁶Pa・sのテトラフルオロエチレン系ポリマーを含むポリマー層とを有する積層体の前記金属箔層を除去して、残存する前記ポリマー層をポリマーフィルムとする、ポリマーフィルムの製造方法。
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2020569583A JP7230932B2 (ja) | 2019-01-30 | 2020-01-24 | 積層体及びその製造方法、複合積層体の製造方法、並びにポリマーフィルムの製造方法 |
| CN202080011655.2A CN113365804A (zh) | 2019-01-30 | 2020-01-24 | 层叠体及其制造方法、复合层叠体的制造方法以及聚合物膜的制造方法 |
| KR1020217023787A KR102865559B1 (ko) | 2019-01-30 | 2020-01-24 | 적층체 및 그 제조 방법, 복합 적층체의 제조 방법, 그리고 폴리머 필름의 제조 방법 |
Applications Claiming Priority (8)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2019-014510 | 2019-01-30 | ||
| JP2019014509 | 2019-01-30 | ||
| JP2019014510 | 2019-01-30 | ||
| JP2019044625 | 2019-03-12 | ||
| JP2019-044625 | 2019-03-12 | ||
| JP2019-014509 | 2019-06-28 | ||
| JP2019192671 | 2019-10-23 | ||
| JP2019-192671 | 2019-10-23 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2020158604A1 true WO2020158604A1 (ja) | 2020-08-06 |
Family
ID=71839973
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2020/002517 Ceased WO2020158604A1 (ja) | 2019-01-30 | 2020-01-24 | 積層体及びその製造方法、複合積層体の製造方法、並びにポリマーフィルムの製造方法 |
Country Status (5)
| Country | Link |
|---|---|
| JP (1) | JP7230932B2 (ja) |
| KR (1) | KR102865559B1 (ja) |
| CN (1) | CN113365804A (ja) |
| TW (1) | TWI850322B (ja) |
| WO (1) | WO2020158604A1 (ja) |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2022145352A1 (ja) * | 2020-12-28 | 2022-07-07 | 株式会社ダイセル | 化合物、接合剤、接合体、プリント基板、及び、接合体の製造方法 |
| US11549035B2 (en) | 2020-12-16 | 2023-01-10 | Saint-Gobain Performance Plastics Corporation | Dielectric substrate and method of forming the same |
| US11596064B2 (en) | 2020-07-28 | 2023-02-28 | Saint-Gobain Performance Plastics Corporation | Dielectric substrate and method of forming the same |
| US12173201B2 (en) | 2020-12-16 | 2024-12-24 | Versiv Composites Limited | Copper-clad laminate and method of forming the same |
| US12262468B2 (en) | 2020-07-28 | 2025-03-25 | Versiv Composites Limited | Copper-clad laminate and method of forming the same |
| US12391850B2 (en) | 2020-12-16 | 2025-08-19 | Versiv Composites Limited | Dielectric substrate and method of forming the same |
| TWI924751B (zh) | 2020-12-28 | 2026-05-11 | 日商大賽璐股份有限公司 | 化合物、黏合劑、黏合體、印刷基板以及黏合體之製造方法 |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116406078B (zh) * | 2023-03-30 | 2025-07-22 | 广州方邦电子股份有限公司 | 金属箔的承载体、金属箔及其应用 |
| CN116321700A (zh) * | 2023-03-30 | 2023-06-23 | 广州方邦电子股份有限公司 | 金属箔的承载体、金属箔及其应用 |
| CN120414053A (zh) * | 2025-04-26 | 2025-08-01 | 苏州世沃电子科技有限公司 | 一种金属箔天线的制作方法 |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2013042781A1 (ja) * | 2011-09-22 | 2013-03-28 | ダイキン工業株式会社 | 積層体及び積層体の製造方法 |
| WO2014126193A1 (ja) * | 2013-02-14 | 2014-08-21 | 三井金属鉱業株式会社 | 表面処理銅箔及び表面処理銅箔を用いて得られる銅張積層板 |
| WO2016159102A1 (ja) * | 2015-04-01 | 2016-10-06 | 三菱鉛筆株式会社 | フッ素系樹脂含有非水系分散体、フッ素系樹脂含有ポリイミド前駆体溶液組成物、それを用いたポリイミド、ポリイミドフィルム、回路基板用接着剤組成物、およびそれらの製造方法 |
| WO2017222027A1 (ja) * | 2016-06-23 | 2017-12-28 | 旭硝子株式会社 | フッ素樹脂パウダーを含む液状組成物の製造方法 |
| JP2018090903A (ja) * | 2016-12-05 | 2018-06-14 | Jx金属株式会社 | 表面処理銅箔、キャリア付銅箔、積層体、プリント配線板の製造方法及び電子機器の製造方法 |
| WO2018212285A1 (ja) * | 2017-05-18 | 2018-11-22 | Agc株式会社 | フッ素樹脂フィルムおよび積層体、ならびに、熱プレス積層体の製造方法 |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP4295800B2 (ja) | 2002-05-13 | 2009-07-15 | 三井金属鉱業株式会社 | 電解銅箔 |
| JP4958045B2 (ja) | 2006-10-27 | 2012-06-20 | 三井金属鉱業株式会社 | フレキシブル銅張積層板製造用の表面処理銅箔及びその表面処理銅箔を用いて得られるフレキシブル銅張積層板 |
| WO2014192718A1 (ja) | 2013-05-31 | 2014-12-04 | 住友電気工業株式会社 | 金属樹脂複合体、配線材及び金属樹脂複合体の製造方法 |
| JP6687409B2 (ja) | 2016-02-09 | 2020-04-22 | 福田金属箔粉工業株式会社 | 高彩度処理銅箔及び該処理銅箔を用いた銅張積層板並びに該処理銅箔の製造方法 |
| JP6728529B2 (ja) | 2016-07-15 | 2020-07-22 | 住友電工ファインポリマー株式会社 | プリプレグ及び多層基板 |
| US10820414B2 (en) * | 2016-12-05 | 2020-10-27 | Jx Nippon Mining & Metals Corporation | Surface treated copper foil, copper foil with carrier, laminate, method for manufacturing printed wiring board, and method for manufacturing electronic device |
-
2020
- 2020-01-24 CN CN202080011655.2A patent/CN113365804A/zh active Pending
- 2020-01-24 JP JP2020569583A patent/JP7230932B2/ja active Active
- 2020-01-24 KR KR1020217023787A patent/KR102865559B1/ko active Active
- 2020-01-24 WO PCT/JP2020/002517 patent/WO2020158604A1/ja not_active Ceased
- 2020-01-30 TW TW109102861A patent/TWI850322B/zh active
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2013042781A1 (ja) * | 2011-09-22 | 2013-03-28 | ダイキン工業株式会社 | 積層体及び積層体の製造方法 |
| WO2014126193A1 (ja) * | 2013-02-14 | 2014-08-21 | 三井金属鉱業株式会社 | 表面処理銅箔及び表面処理銅箔を用いて得られる銅張積層板 |
| WO2016159102A1 (ja) * | 2015-04-01 | 2016-10-06 | 三菱鉛筆株式会社 | フッ素系樹脂含有非水系分散体、フッ素系樹脂含有ポリイミド前駆体溶液組成物、それを用いたポリイミド、ポリイミドフィルム、回路基板用接着剤組成物、およびそれらの製造方法 |
| WO2017222027A1 (ja) * | 2016-06-23 | 2017-12-28 | 旭硝子株式会社 | フッ素樹脂パウダーを含む液状組成物の製造方法 |
| JP2018090903A (ja) * | 2016-12-05 | 2018-06-14 | Jx金属株式会社 | 表面処理銅箔、キャリア付銅箔、積層体、プリント配線板の製造方法及び電子機器の製造方法 |
| WO2018212285A1 (ja) * | 2017-05-18 | 2018-11-22 | Agc株式会社 | フッ素樹脂フィルムおよび積層体、ならびに、熱プレス積層体の製造方法 |
Cited By (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11596064B2 (en) | 2020-07-28 | 2023-02-28 | Saint-Gobain Performance Plastics Corporation | Dielectric substrate and method of forming the same |
| US11805600B2 (en) | 2020-07-28 | 2023-10-31 | Saint-Gobain Performance Plastics Corporation | Dielectric substrate and method of forming the same |
| US12250767B2 (en) | 2020-07-28 | 2025-03-11 | Versiv Composites Limited | Dielectric substrate and method of forming the same |
| US12262468B2 (en) | 2020-07-28 | 2025-03-25 | Versiv Composites Limited | Copper-clad laminate and method of forming the same |
| US11549035B2 (en) | 2020-12-16 | 2023-01-10 | Saint-Gobain Performance Plastics Corporation | Dielectric substrate and method of forming the same |
| US12049577B2 (en) | 2020-12-16 | 2024-07-30 | Versiv Composites Limited | Dielectric substrate and method of forming the same |
| US12173201B2 (en) | 2020-12-16 | 2024-12-24 | Versiv Composites Limited | Copper-clad laminate and method of forming the same |
| US12391850B2 (en) | 2020-12-16 | 2025-08-19 | Versiv Composites Limited | Dielectric substrate and method of forming the same |
| WO2022145352A1 (ja) * | 2020-12-28 | 2022-07-07 | 株式会社ダイセル | 化合物、接合剤、接合体、プリント基板、及び、接合体の製造方法 |
| JPWO2022145352A1 (ja) * | 2020-12-28 | 2022-07-07 | ||
| TWI924751B (zh) | 2020-12-28 | 2026-05-11 | 日商大賽璐股份有限公司 | 化合物、黏合劑、黏合體、印刷基板以及黏合體之製造方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| CN113365804A (zh) | 2021-09-07 |
| TWI850322B (zh) | 2024-08-01 |
| JPWO2020158604A1 (ja) | 2021-12-02 |
| TW202037488A (zh) | 2020-10-16 |
| KR102865559B1 (ko) | 2025-09-26 |
| JP7230932B2 (ja) | 2023-03-01 |
| KR20210121048A (ko) | 2021-10-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP7230932B2 (ja) | 積層体及びその製造方法、複合積層体の製造方法、並びにポリマーフィルムの製造方法 | |
| TWI766021B (zh) | 氟樹脂膜及積層體以及熱壓積層體之製造方法 | |
| TWI824049B (zh) | 分散液 | |
| CN112236302B (zh) | 带树脂的金属箔的制造方法、带树脂的金属箔、层叠体及印刷基板 | |
| JP2020180245A (ja) | パウダー分散液、積層体の製造方法、積層体及びプリント基板の製造方法 | |
| TWI814836B (zh) | 分散液、附樹脂之金屬箔之製造方法、及印刷基板之製造方法 | |
| KR20210016327A (ko) | 수지 부착 금속박의 제조 방법 및 수지 부착 금속박 | |
| JP2020158720A (ja) | 複合粒子、分散液、積層体の製造方法、膜の製造方法及び被覆織布の製造方法 | |
| WO2021075504A1 (ja) | 非水系分散液及び積層体の製造方法 | |
| JP2021075030A (ja) | 積層体、積層体の製造方法、シート、及びプリント回路基板 | |
| TW201945208A (zh) | 積層體之製造方法及積層體 | |
| WO2020059606A1 (ja) | 積層体、プリント基板及びその製造方法 | |
| WO2020004338A1 (ja) | 樹脂付金属箔 | |
| KR102897538B1 (ko) | 액상 조성물 | |
| JP2020070401A (ja) | 分散液 | |
| JP2020055241A (ja) | 樹脂付金属箔及び樹脂付金属箔の製造方法 | |
| KR102787276B1 (ko) | 적층체 및 적층체의 제조 방법 | |
| JP7452534B2 (ja) | パウダー分散液、パウダー分散液の製造方法及び樹脂付基板の製造方法 | |
| JP2020083990A (ja) | 複合体の製造方法及び複合体 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 20748570 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2020569583 Country of ref document: JP Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 20748570 Country of ref document: EP Kind code of ref document: A1 |