WO2018043443A1 - 二次電池用電極及びその製造方法、並びに二次電池及びその製造方法 - Google Patents
二次電池用電極及びその製造方法、並びに二次電池及びその製造方法 Download PDFInfo
- Publication number
- WO2018043443A1 WO2018043443A1 PCT/JP2017/030827 JP2017030827W WO2018043443A1 WO 2018043443 A1 WO2018043443 A1 WO 2018043443A1 JP 2017030827 W JP2017030827 W JP 2017030827W WO 2018043443 A1 WO2018043443 A1 WO 2018043443A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- electrode
- active material
- material layer
- secondary battery
- core
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images


Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M4/00—Electrodes
- H01M4/02—Electrodes composed of, or comprising, active material
- H01M4/04—Processes of manufacture in general
- H01M4/043—Processes of manufacture in general involving compressing or compaction
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/08—Devices involving relative movement between laser beam and workpiece
- B23K26/082—Scanning systems, i.e. devices involving movement of the laser beam relative to the laser head
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/08—Devices involving relative movement between laser beam and workpiece
- B23K26/083—Devices involving movement of the workpiece in at least one axial direction
- B23K26/0838—Devices involving movement of the workpiece in at least one axial direction by using an endless conveyor belt
- B23K26/0846—Devices involving movement of the workpiece in at least one axial direction by using an endless conveyor belt for moving elongated workpieces longitudinally, e.g. wire or strip material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/36—Removing material
- B23K26/38—Removing material by boring or cutting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/36—Removing material
- B23K26/40—Removing material taking account of the properties of the material involved
- B23K26/402—Removing material taking account of the properties of the material involved involving non-metallic material, e.g. isolators
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/05—Accumulators with non-aqueous electrolyte
- H01M10/052—Li-accumulators
- H01M10/0525—Rocking-chair batteries, i.e. batteries with lithium insertion or intercalation in both electrodes; Lithium-ion batteries
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M4/00—Electrodes
- H01M4/02—Electrodes composed of, or comprising, active material
- H01M4/04—Processes of manufacture in general
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M4/00—Electrodes
- H01M4/02—Electrodes composed of, or comprising, active material
- H01M4/13—Electrodes for accumulators with non-aqueous electrolyte, e.g. for lithium-accumulators; Processes of manufacture thereof
- H01M4/139—Processes of manufacture
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M50/00—Constructional details or processes of manufacture of the non-active parts of electrochemical cells other than fuel cells, e.g. hybrid cells
- H01M50/50—Current conducting connections for cells or batteries
- H01M50/531—Electrode connections inside a battery casing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K2101/00—Articles made by soldering, welding or cutting
- B23K2101/36—Electric or electronic devices
- B23K2101/38—Conductors
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K2103/00—Materials to be soldered, welded or cut
- B23K2103/08—Non-ferrous metals or alloys
- B23K2103/10—Aluminium or alloys thereof
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K2103/00—Materials to be soldered, welded or cut
- B23K2103/08—Non-ferrous metals or alloys
- B23K2103/12—Copper or alloys thereof
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K2103/00—Materials to be soldered, welded or cut
- B23K2103/16—Composite materials
- B23K2103/166—Multilayered materials
- B23K2103/172—Multilayered materials wherein at least one of the layers is non-metallic
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
Definitions
- the present disclosure relates to an electrode for a secondary battery and a manufacturing method thereof, and a secondary battery and a manufacturing method thereof.
- Patent Document 1 discloses a technique for cutting a long electrode precursor into a predetermined shape using a laser. In the technique of Patent Document 1, a pulse laser oscillator is used.
- An electrode for a secondary battery according to the present disclosure includes a core body and an active material layer formed on at least one surface of the core body, and an angle formed between an end surface of the active material layer and the surface of the core body is 55 °. It is ⁇ 85 °, and protrusion marks are present on the end face of the active material layer or in the vicinity thereof.
- an active material layer is formed using a first step of forming an active material layer on at least one surface of a long core and a continuous wave laser. And a second step of cutting the electrode precursor, which is a long core, into a predetermined shape.
- an electrode for a secondary battery According to the method for manufacturing an electrode for a secondary battery according to the present disclosure, it is possible to stably manufacture an electrode having a straight and clean cut portion at a high speed.
- the importance of improving the productivity of the electrode by cutting the electrode precursor cleanly at high speed is increasing, but the conventional using a cutter or the like has increased. It is difficult to cut the electrode precursor at a high speed by a general cutting method. Further, in the cutting method using a pulse laser as disclosed in Patent Document 1, the cut portion of the electrode precursor has a wavy shape, and it is difficult to cleanly cut it into a straight line. Further, when a pulse laser is used, there is a problem that the active material layer is removed at the cut portion and the surface of the core body is easily exposed.
- a linear clean cut portion is formed at high speed by cutting the electrode precursor using a continuous wave laser (CW laser).
- CW laser continuous wave laser
- Electrode productivity can be greatly improved.
- protrusions that may cause a short circuit between the positive and negative electrodes are easily formed on or near the end face of the active material layer.
- the protrusions can be adjusted by adjusting the laser irradiation conditions or by the compression process of the active material layer. Or can be made small to the extent that battery performance is not affected.
- the secondary battery electrode 10 applied to the stacked electrode body is exemplified, but the secondary battery electrode according to the present disclosure may be applied to a wound electrode body, and the manufacturing method according to the present disclosure. Can also be applied to the production of an electrode for a wound electrode body.
- FIG. 1 is a front view showing a secondary battery electrode 10 which is an example of an embodiment, and also shows a cross-sectional view of an electrode end portion.
- the secondary battery electrode 10 includes a core body 11 and active material layers 12 formed on both surfaces of the core body 11.
- the active material layer 12 may be formed only on one surface of the core body 11, but is preferably formed on both surfaces of the core body 11.
- the secondary battery electrode 10 may be either a positive electrode or a negative electrode. However, the positive electrode and the negative electrode have different electrode sizes, such as the material constituting the core 11 and the active material contained in the active material layer 12, as described later.
- the secondary battery electrode 10 has a base portion 13 and a lead portion 14 protruding from one end of the base portion 13.
- the base portion 13 and the lead portion 14 are integrally formed.
- the base portion 13 is a portion where the active material layer 12 is formed, and the active material layer 12 is formed on both sides of the core body 11.
- the base portion 13 has a rectangular shape in front view that is long in the lateral direction, but the shape is not particularly limited.
- the lead portion 14 protrudes from one end in the long side direction on one end side in the short side direction of the base portion 13 and has a rectangular shape in front view.
- the active material layer 12 is generally formed at the base of the lead portion 14, but is not formed on the majority of the lead portion 14.
- the secondary battery electrode 10 is applied to a laminated electrode body.
- the stacked electrode body is an electrode body having a plurality of positive electrodes and a plurality of negative electrodes, and the positive electrodes and the negative electrodes are alternately stacked via separators.
- the secondary battery electrode 10 is a positive electrode, a plurality of positive electrode lead portions 14 laminated via a separator and a negative electrode are joined together by welding or the like.
- reed part 14 is connected to the positive electrode terminal of a battery directly or through a metal current collection member.
- the secondary battery to which the secondary battery electrode 10 is applied is a nonaqueous electrolyte secondary battery such as a lithium ion battery, but is not limited thereto.
- the secondary battery include a rectangular battery having a rectangular metal case, and a laminated battery having an exterior body made of a metal layer laminate film, but may be other types of batteries.
- description will be made assuming that the secondary battery electrode 10 is applied to a lithium ion battery.
- the core 11 (positive electrode current collector) has a metal foil that is stable in the potential range of the positive electrode such as aluminum or aluminum alloy, a film in which the metal is disposed on the surface layer, or the like. Can be used.
- the thickness of the positive electrode current collector is, for example, 5 ⁇ m to 30 ⁇ m.
- the active material layer 12 is a positive electrode mixture layer
- the active material layer 12 generally includes a positive electrode active material such as a lithium-containing transition metal oxide, a conductive material, and a binder.
- the thickness of the positive electrode mixture layer is, for example, preferably 20 ⁇ m to 200 ⁇ m on one side of the positive electrode current collector, and more preferably 50 ⁇ m to 150 ⁇ m.
- the conductive material is preferably a carbon material or the like
- the binder is preferably polyvinylidene fluoride or the like.
- the core 11 (negative electrode current collector) has a metal foil that is stable in the potential range of the negative electrode such as copper or copper alloy, a film in which the metal is disposed on the surface layer, or the like. Can be used.
- the thickness of the negative electrode current collector is, for example, 5 ⁇ m to 30 ⁇ m.
- the active material layer 12 is a negative electrode composite material layer, the active material layer 12 is generally made of a carbon material such as natural graphite or artificial graphite, a metal alloyed with lithium such as Si or Sn, an alloy, or a composite oxide. Negative electrode active materials such as, and binders.
- the thickness of the negative electrode mixture layer is, for example, preferably 20 ⁇ m to 200 ⁇ m on one side of the negative electrode current collector, and more preferably 50 ⁇ m to 150 ⁇ m.
- the binder is preferably a rubber-based binder such as styrene butadiene rubber.
- the secondary battery electrode 10 has a straight and clean cut portion.
- the angle ⁇ 1 formed by the end surface 12e of the active material layer 12 on one side and the core surface 11s is preferably 55 ° to 85 °.
- the angle ⁇ 1 is substantially the same as the angle ⁇ 2 formed by the surface of the opposite side active material layer 22 and the end face 22e.
- the projection trace 15 is a trace of the projection 25 described later, and is observed as a massive portion (particulate portion) having a contrast different from that of other portions by, for example, a scanning electron microscope (SEM).
- the protrusion marks 15 are embedded in the active material layer 12, but may be raised on the active material layer 12 at a height that does not affect the battery performance.
- the size of the protrusion mark 15 is preferably 30 ⁇ m to 300 ⁇ m, and more preferably 30 ⁇ m to 150 ⁇ m, in a cross section perpendicular to the laser scanning direction, for example, the cross section shown in FIG.
- the protrusion mark 15 is formed, for example, by compressing the protrusion 25 in an active material layer compression step described later.
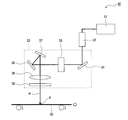
- FIG. 2 shows the overall configuration of the laser system 30.
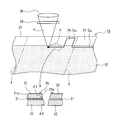
- 2 and 3 show a state in which the electrode precursor 20 is cut by the laser light ⁇ output from the laser system 30.
- the member used as the core 11 of the electrode 10 for secondary batteries by cutting the electrode precursor 20 be the elongate core 21, and the layer used as the active material layer 12 be the active material layer 22.
- the secondary battery electrode 10 is obtained by cutting a long electrode precursor 20 in which an active material layer 22 is formed on both surfaces of a long core 21 into a predetermined shape.
- the manufacturing process of the secondary battery electrode 10 includes a first process of forming the active material layer 22 on at least one surface of the elongated core body 21 and an electrode precursor 20 using a continuous wave laser (CW laser). And a second step of cutting.
- active material layers 22 are formed on both surfaces of the elongated core 21 in the first step.
- a mixture slurry containing the constituent material of the active material layer 22 is prepared, the slurry is applied to both surfaces of the elongated core body 21, and the coating film is dried to form the active material layer 22. .
- the exposed portion 23 where the core surface 21 s is exposed is formed along the longitudinal direction of the electrode precursor 20.
- the exposed portion 23 is preferably formed with a substantially constant width from one end in the width direction of the long core 21.
- the width of the exposed portion 23 is, for example, 1/5 or less of the width of the long core 21.
- the exposed portion 23 may be formed by forming the active material layer 22 on both sides of the long core 21 and then peeling and removing a part of the active material layer 22. It is formed by not applying the mixture slurry to a part of the body 21.
- the elongate core 21 has a width capable of forming two secondary battery electrodes 10 in the width direction, for example. In this case, exposed portions 23 are formed at both ends in the width direction of the electrode precursor 20.
- the electrode precursor 20 is irradiated with the laser beam ⁇ output from the laser system 30 to cut the electrode precursor 20 into a predetermined shape.
- the electrode precursor 20 is irradiated with the laser beam ⁇ while the relative position between the electrode precursor 20 and the processing head of the laser system 30 is changed.
- a cutting process may be performed while the electrode precursor 20 is being conveyed.
- the laser beam ⁇ may be scanned while conveying the electrode precursor 20.
- the laser system 30 includes a laser oscillator 31 and a processing head that incorporates a galvano scanner 33.
- the laser oscillator 31 is an oscillator capable of continuous oscillation.
- Examples of the laser oscillator 31 include a YAG laser, a CO 2 laser, an Ar laser, and a fiber laser that can output the laser light ⁇ in the continuous oscillation mode.
- a suitable example is a fiber laser.
- An example of a preferable range of the oscillation wavelength is 900 nm to 1200 nm.
- a collimator 32 is provided between the laser oscillator 31 and the galvano scanner 33 so that the laser light ⁇ output from the laser oscillator 31 is a parallel beam.
- the galvano scanner 33 includes, in order from the laser oscillator 31 side, a reflection mirror 34, an optical element 35, an X-axis mirror 36, a Y-axis mirror 37, and an F ⁇ lens 38.
- a reflection mirror 34 for example, a diffraction grating or the like is used.
- the laser light ⁇ which is a continuous wave that has passed through the collimator 32 is bent toward the optical element 35 by the reflection mirror 34, passes through the optical element 35, and is guided to the X-axis mirror 36 and the Y-axis mirror 37.
- the laser beam ⁇ can be scanned, and the position of the irradiation spot P can be changed in the two-dimensional plane.
- the laser light ⁇ reflected by the X-axis mirror 36 and the Y-axis mirror 37 is irradiated to the electrode precursor 20 through the F ⁇ lens 38 and the protective glass 39.
- a portion of the electrode precursor 20 provided with the active material layer 22 is cut along the exposed portion 23 using a continuous wave laser, and cut at a substantially constant period.
- a convex portion 24 to be the lead portion 14 is formed.
- the laser beam ⁇ can be applied to the boundary position between the portion where the active material layer 22 is provided and the exposed portion 23.
- the surface of the core body is applied to a portion other than the lead portion 14 due to slight deviation of the irradiation spot P. An exposed portion of 11s is formed.
- the exposed portion formed in a portion other than the lead portion 14 may cause a low-resistance short circuit between the positive and negative electrodes, it is preferable to cut the electrode precursor 20 so that the exposed portion is not formed particularly in the positive electrode. . For this reason, it is preferable to cut the electrode precursor 20 by irradiating the portion where the active material layer 22 near the exposed portion 23 is provided with the laser beam ⁇ .
- the laser beam ⁇ is scanned along the exposed portion 23 (longitudinal direction of the electrode precursor 20), and is scanned toward the exposed portion 23 (width direction of the electrode precursor 20) at a portion corresponding to the convex portion 24. Since the laser beam ⁇ is continuously irradiated even at the boundary position between the portion where the active material layer 22 is provided and the exposed portion 23, the cut portion C 22 where the active material layer 22 is provided and the exposed portion 23. the cut portion C 23 of, are formed into a continuous single linear. By cutting the exposed portion 23 while changing the cutting direction at a substantially constant cycle, a plurality of convex portions 24 arranged at substantially equal intervals in the longitudinal direction of the electrode precursor 20 are formed. And the electrode 10 for secondary batteries which has the base 13 in which the active material layer 12 was formed in the whole, and the lead part 14 in which the active material layer 12 was formed in the root is obtained.
- the electrode precursor 20 may be cut into an electrode size using a continuous wave laser.
- the electrode precursor 20 is cut along the longitudinal direction at the center.
- an electrode precursor 20 cut to a width corresponding to one electrode 10 for a secondary battery is obtained.
- a continuous wave laser is used for the cutting step. Is preferred.
- the electrode precursor 20 having a size adjusted to a width corresponding to one secondary battery electrode 10 may be supplied to the compression step of the active material layer 22.
- the active material layer may be compressed after the electrode precursor 20 is cut at the planned cutting portion X to obtain individual electrode sizes.
- the step of cutting the electrode precursor 20 at the planned cutting portion X may be performed using a continuous wave laser, or may be performed using a conventional general cutting method using a cutter or the like.
- FIG. 4 is a scanning electron microscope (SEM) photograph taken of a cross section of the cut portion C 22 of the electrode precursor 20 and the vicinity thereof.
- SEM scanning electron microscope
- the protrusion height of the protrusion 25 from the upper surface of the active material layer 22 is preferably 10 ⁇ m to 100 ⁇ m, and more preferably 10 ⁇ m to 80 ⁇ m.
- the protrusion 25 is formed on the surface of the active material layer 22 on the side on which the laser beam ⁇ is incident first.
- Such protrusions 25 are preferably removed because they may cause a short circuit between the positive and negative electrodes.
- the protrusion 25 can be embedded in the active material layer 22, or the protrusion 25 can be dropped from the active material layer 22. Further, the formation of the protrusions 25 can be suppressed by controlling the laser irradiation conditions.
- the angle ⁇ 1 formed by the end surface 22e of the active material layer 22 on the side on which the laser light ⁇ first enters and the core surface 21s is
- the angle is preferably 55 ° to 85 °.
- the core surface 21 s is not covered with the active material layer 22 and is not exposed, and both the cut portions C 22 and C 23 become a beautiful straight cut portion.
- the angle ⁇ 1 is preferably substantially the same as the angle ⁇ 2 formed by the surface of the opposite side active material layer 22 and the end face 22e, for example.
- the laser irradiation conditions are preferably adjusted based on the material, thickness, cut shape, and the like of the long core 21 and the active material layer 22, but generally the output of the continuous wave laser (laser oscillator 31) is 500 W to 5000 W.
- the spot diameter of the laser beam ⁇ is preferably 5 ⁇ m to 100 ⁇ m.
- the cutting speed of the electrode precursor 20 by the continuous wave laser is preferably set to, for example, 500 mm / s to 8000 mm / s. Irradiation conditions may be changed depending on whether the electrode precursor 20 is a positive electrode precursor or a negative electrode precursor. In general, the positive electrode precursor is easier to cut.
- the laser output is preferably 1000W to 3000W.
- the spot diameter is preferably 10 ⁇ m to 100 ⁇ m, more preferably 10 ⁇ m to 40 ⁇ m.
- the cutting speed is more preferably 1000 mm / s to 5000 mm / s.
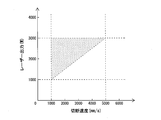
- FIG. 5 is a diagram showing the relationship between laser output and cutting speed.
- the laser output is preferably 1000 W to 3000 W and the cutting speed is preferably 1000 mm / s to 5000 mm / s, but the laser output and the cutting speed are more preferably in a relationship indicated by a triangle in FIG. That is, the first point of laser output: 1000 W, cutting speed: 1000 mm / s, the second point of laser output: 3000 W, cutting speed: 1000 mm / s, the laser output: 3000 W, the cutting speed: 5000 mm / s. It is preferable to adjust the laser output and the cutting speed so as to fall within a triangle whose vertex is the third point.
- the laser output and the cutting speed within the range indicated by the triangle in FIG. 5, it becomes easy to form a straight and clean cut portion, and the formation of the protrusion 25 can be suppressed. Moreover, if the cutting speed is 1000 mm / s or more, good productivity can be secured.
- irradiation conditions are appropriately changed within the range of the triangle according to the material, thickness, cut shape, and the like of the long core 21 and the active material layer 22. For example, when a condition close to the third point with a laser output of 3000 W and a cutting speed of 5000 mm / s is applied, cutting can be performed at a higher speed than when other conditions close to the two points are applied. There is a tendency that the cut portion becomes rough. For this reason, when the cutting shape is simple, a condition close to the third point may be applied.
- the manufacturing process of the secondary battery electrode 10 further includes a process of compressing the active material layer cut by the continuous wave laser.
- the compression of the active material layer is performed using, for example, a rolling roller that sandwiches the electrode precursor 20 from both sides.
- the compression step of the active material layer may be performed before the second step, which is a cutting step of the electrode precursor 20, but is preferably performed after the second step.
- the compression process is performed after the second process, even if the protrusion 25 is formed by cutting with a continuous wave laser, the protrusion 25 is crushed and embedded in the active material layer, or the protrusion 25 is dropped from the active material layer. be able to.
- the compression process may be performed after the electrode precursor 20 is cut into individual electrode sizes. However, in consideration of productivity, for example, an electrode whose size is adjusted to a width corresponding to one electrode 10 for a secondary battery It is preferably performed in the state of the precursor 20. And it is preferable to cut
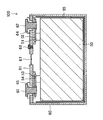
- an electrode body 50 in which a plurality of positive electrodes and a plurality of negative electrodes are alternately stacked via a separator is formed in a battery case 60 together with an electrolytic solution (not shown).
- the electrode 10 for secondary batteries is used as a positive electrode or a negative electrode.
- the opening of the battery case 60 is sealed with a sealing body 61.
- the positive electrode terminal 62 and the negative electrode terminal 63 are fixed to the sealing body 61 via resin members 64 and 65, respectively.
- the positive electrode is electrically connected to the positive electrode terminal 62 via the positive electrode lead portion 51 and the positive electrode current collecting member 52.
- the negative electrode is electrically connected to the negative electrode terminal 63 via the negative electrode lead portion 53 and the negative electrode current collecting member 54.
- the sealing body 61 is provided with a liquid injection hole for injecting an electrolytic solution.
- the liquid injection hole is sealed with a sealing member 66 after the electrolytic solution is injected.
- the sealing body 61 is provided with a gas discharge valve 67 for releasing the pressure when the internal pressure of the battery case 60 rises.
- the electrode body 50 is preferably disposed in the battery case 60 in a state where the electrode body 50 is disposed inside the box-shaped or bag-shaped insulating sheet 55.
- the positive electrode lead portion 51 protruding from each positive electrode is in a curved state and connected to a portion of the positive electrode current collecting member 52 that is disposed substantially parallel to the sealing body 61.
- the negative electrode lead portion 53 protruding from each negative electrode is in a curved state and connected to a portion of the negative electrode current collecting member 54 that is disposed substantially parallel to the sealing body 61.
- the positive electrode or the negative electrode manufactured by the above method having an end face cut by a continuous wave laser is bonded to a separator disposed between the positive electrode and the negative electrode.
- an adhesion method it is preferable to provide an adhesive layer on the surface of a separator made of polyolefin such as polypropylene or polyethylene, or on the surface of the active material layer of the electrode, and bond the separator and the active material layer with this adhesive layer.
- the adhesive layer is not particularly limited, but is preferably a layer softer than the separator.
- the adhesive layer is preferably made of a resin, and for example, polyvinylidene fluoride, carboxymethyl cellulose, polyvinyl alcohol, or the like can be used.
- the adhesive layer is preferably in contact with the projection mark 15. Thereby, when using a secondary battery, it can prevent that the protrusion trace 15 slips off from an active material layer.
- the electrolyte solution may not easily penetrate into the active material layer.
- the angle ⁇ 1 formed between the end surface 12e of the active material layer 12 and the core surface 11s is 55 ° to 85 °, the area of the end surface of the active material layer increases, and therefore the inside of the active material layer It becomes easy for the electrolyte solution to penetrate into.
- a protective layer made of ceramic particles such as alumina, zirconia, and titania and a binder may be provided in a portion adjacent to the active material layer 22 in the lead portion 14.
- the protective layer can also contain a conductive material such as a carbon material.
- the method for producing a secondary battery electrode according to the present disclosure is applied as a method for producing a positive electrode or a negative electrode, which is used for a wound electrode body in which a long positive electrode and a long negative electrode are wound through a separator. It is possible. In this case, a plurality of positive electrode lead portions provided on the positive electrode and a plurality of negative electrode lead portions provided on the negative electrode are disposed on one end side in the direction in which the winding axis of the wound electrode body extends. It is preferable to do so. Thereby, it becomes a secondary battery with higher volume energy density.
- the plurality of positive electrode lead portions provided on the long positive electrode are preferably formed at different intervals so that the plurality of positive electrode lead portions are stacked in the wound electrode body, not at equal intervals. .
- An elongate positive electrode has an active material layer formed on both sides of the core, and the amount of the active material layer of the active material layer on one side (the upper active material layer in FIG. 1) is the other side.
- the amount of the active material layer on the side (the lower active material layer in FIG. 1) is smaller, the active material layer on the one side with the smaller amount of the active material layer is disposed on the winding center side of the wound electrode body It is preferable to do so.
- the amount of the negative electrode active material layer located inside the positive electrode is usually smaller than the amount of the negative electrode active material layer located outside. Therefore, in the above-described configuration, the opposing balance between the positive electrode active material layer and the negative electrode active material layer is more preferable.
- SYMBOLS 10 Secondary battery electrode, 11 core, 11s core surface, 12 active material layer, 12e, 22e end face, 13 base, 14 lead part, 15 projection trace, 20 electrode precursor, 21 long core, 21s Core surface, 22 active material layer, 22e end face, 23 exposed part, 24 convex part, 25 protrusion, 30 laser system, 31 laser oscillator, 32 collimator, 33 galvano scanner, 34 reflecting mirror, 35 optical element, 36 X axis mirror , 37 Y-axis mirror, 38 F ⁇ lens, 39 protective glass, 100 secondary battery, C 22 , C 23 cutting part, ⁇ laser beam, P irradiation spot, X cutting scheduled part
Landscapes
- Engineering & Computer Science (AREA)
- Optics & Photonics (AREA)
- Physics & Mathematics (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Electrochemistry (AREA)
- Plasma & Fusion (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Materials Engineering (AREA)
- Battery Electrode And Active Subsutance (AREA)
- Laser Beam Processing (AREA)
- Connection Of Batteries Or Terminals (AREA)
Abstract
直線状の綺麗な切断部を有する二次電池用電極を高速で安定に製造できる二次電池用電極の製造方法を提供する。実施形態の一例である二次電池用電極(10)の製造方法は、長尺状芯体(21)の少なくとも一方の面に活物質層(22)を形成する第1工程を含む。さらに、実施形態の一例である二次電池用電極(10)の製造方法は、連続発振レーザを用いて、活物質層(22)が形成された長尺状芯体(21)である電極前駆体(20)を所定の形状に切断する第2工程とを含む。
Description
本開示は、二次電池用電極及びその製造方法、並びに二次電池及びその製造方法に関する。
二次電池に使用される電極は、例えば長尺状の芯体に活物質層を形成した後、当該芯体を所定の形状に切断し、個々の電極サイズに切断して製造される。特許文献1には、レーザを用いて長尺状の電極前駆体を所定の形状に切断する技術が開示されている。特許文献1の技術では、パルス方式のレーザ発振器が使用されている。
ところで、電極前駆体を綺麗に高速で切断し、電極の生産性を向上させることは重要な課題である。特に、二次電池の高容量化に伴い、積層型電極体の電極積層数が増加し、或いは巻回型電極体の電極巻回数が増加する傾向にあるため、切断速度の高速化に対する要求は高まっている。しかしながら、特許文献1の技術を含む従来の技術では、電極前駆体を綺麗に高速で切断することは困難であった。
本開示に係る二次電池用電極は、芯体と、芯体の少なくとも一方の面に形成された活物質層とを備え、活物質層の端面と芯体の表面とがなす角度が55°~85°であり、活物質層の端面又はその近傍には突起痕が存在することを特徴とする。
本開示に係る二次電池用電極の製造方法は、長尺状芯体の少なくとも一方の面に活物質層を形成する第1工程と、連続発振レーザを用いて、活物質層が形成された長尺状芯体である電極前駆体を所定の形状に切断する第2工程とを含むことを特徴とする。
本開示に係る二次電池用電極の製造方法によれば、直線状の綺麗な切断部を有する電極を高速で安定に製造することができる。
上述のように、二次電池の高容量化に伴い、電極前駆体を綺麗に高速で切断して電極の生産性を向上させることの重要性が高まっているが、カッター等を用いた従来の一般的な切断法では電極前駆体を高速で切断することは難しい。また、上記特許文献1に開示されるようなパルスレーザを用いた切断法では、電極前駆体の切断部が波打った形状となり、直線状に綺麗に切断することが難しい。さらに、パルスレーザを用いた場合は、切断部で活物質層が除去されてしまい芯体の表面が露出し易いといった課題もある。
これに対し、本開示に係る二次電池用電極の製造方法によれば、連続発振レーザ(CWレーザ)を用いて電極前駆体を切断することにより、直線状の綺麗な切断部を高速で形成することができ、電極の生産性が大幅に向上する。連続発振レーザを用いた場合、活物質層の端面又はその近傍に正負極間の短絡の原因となり得る突起が形成され易いが、レーザ照射条件の調整により、或いは活物質層の圧縮工程により、突起を除去又は電池性能に影響がない程度に小さくできる。
以下、図面を参照しながら、本開示に係る二次電池用電極及びその製造方法の実施形態の一例について詳細に説明する。実施形態の説明で参照する図面は、模式的に記載されたものであり、図面に描画された構成要素の寸法などは、現物と異なる場合がある。具体的な寸法等は、以下の説明を参酌して判断されるべきである。本明細書において「略~」との用語は、略同一を例に説明すると、完全に同一はもとより、実質的に同一と認められるものを含む意図である。
以下では、積層型電極体に適用される二次電池用電極10を例示するが、本開示に係る二次電池用電極は巻回型電極体に適用されてもよく、本開示に係る製造方法は巻回型電極体用の電極の製造にも適用できる。
図1は、実施形態の一例である二次電池用電極10を示す正面図であって、電極端部の断面図を併せて示している。図1に例示するように、二次電池用電極10は、芯体11と、芯体11の両面に形成された活物質層12とを備える。活物質層12は、芯体11の一方の面のみに形成されてもよいが、好ましくは芯体11の両面に形成される。二次電池用電極10は、正極、負極のいずれであってもよい。但し、正極と負極では、後述するように、芯体11を構成する材料、活物質層12に含まれる活物質等、電極サイズなどが互いに異なる。
二次電池用電極10は、基部13と、基部13の一端から突出したリード部14とを有する。二次電池用電極10では、基部13とリード部14が一体成形されている。基部13は、活物質層12が形成される部分であって、芯体11の両面の全域に活物質層12が形成されている。基部13は、横方向に長い正面視矩形形状を有するが、その形状は特に限定されない。リード部14は、基部13の短辺方向一端側において長辺方向一端から突出し、正面視矩形形状を有する。活物質層12は、一般的にリード部14の付け根にも形成されるが、リード部14の大部分には形成されない。
二次電池用電極10は、積層型電極体に適用される。積層型電極体は、複数の正極と複数の負極を有し、正極と負極がセパレータを介して交互に積層されてなる電極体である。二次電池用電極10が正極である場合、セパレータと負極を介して積層された複数の正極のリード部14同士が溶接等により接合される。そして、当該リード部14が、直接あるいは金属製の集電部材を介して電池の正極端子に接続される。
二次電池用電極10が適用される二次電池は、例えばリチウムイオン電池等の非水電解質二次電池であるが、これに限定されるものではない。また、二次電池としては、角形の金属製ケースを有する角形電池、金属層ラミネートフィルムで構成された外装体を有するラミネート電池などが例示できるが、他の形態の電池であってもよい。以下では、二次電池用電極10がリチウムイオン電池に適用されるものとして説明する。
二次電池用電極10が正極である場合、芯体11(正極集電体)には、アルミニウムやアルミニウム合金などの正極の電位範囲で安定な金属の箔、当該金属を表層に配置したフィルム等を用いることができる。正極集電体の厚みは、例えば5μm~30μmである。活物質層12が正極合材層である場合、活物質層12には、一般的にリチウム含有遷移金属酸化物等の正極活物質、導電材、及び結着材が含まれる。正極合材層の厚みは、例えば正極集電体の片側で20μm~200μmが好ましく、50μm~150μmがより好ましい。特に限定されないが、導電材は炭素材料等が好ましく、また、結着材はポリフッ化ビニリデン等が好ましい。
二次電池用電極10が負極である場合、芯体11(負極集電体)には、銅や銅合金などの負極の電位範囲で安定な金属の箔、当該金属を表層に配置したフィルム等を用いることができる。負極集電体の厚みは、例えば5μm~30μmである。活物質層12が負極合材層である場合、活物質層12には、一般的に天然黒鉛、人造黒鉛等の炭素材料、Si、Sn等のリチウムと合金化する金属、合金、複合酸化物などの負極活物質、及び結着材が含まれる。負極合材層の厚みは、例えば負極集電体の片側で20μm~200μmが好ましく、50μm~150μmがより好ましい。特に限定されないが、結着材はスチレンブタジエンゴム等のゴム系の結着材等が好ましい。
二次電池用電極10は、直線状の綺麗な切断部を有する。二次電池用電極10では、例えば一方側の活物質層12の端面12eと芯体表面11sとがなす角度θ1が55°~85°となるようにすることが好ましい。角度θ1は、例えば反対側の活物質層22の表面と端面22eとがなす角度θ2と略同一となる。また、端面12e又はその近傍に突起痕15が存在する場合がある。突起痕15は、後述する突起25の痕であって、例えば走査型電子顕微鏡(SEM)により他の部分とコントラストが異なる塊状部分(粒子状部分)として観察される。突起痕15は、活物質層12に埋まっているが、電池性能に影響のない程度の高さで活物質層12上に隆起していてもよい。なお、突出痕15の大きさは、レーザの走査方向に対して垂直な断面、例えば図1に示す断面において、30μm~300μmとすることが好ましく、30μm~150μmとすることがより好ましい。突起痕15は、例えば後述する活物質層の圧縮工程で突起25を圧縮して形成される。
以下、図2~図5を参照しながら、二次電池用電極10の製造方法の一例について詳細に説明する。図2は、レーザシステム30の全体構成を示す。図2及び図3は、レーザシステム30から出力されるレーザ光αにより電極前駆体20を切断する様子を示す。ここでは、電極前駆体20の切断により二次電池用電極10の芯体11となる部材を長尺状芯体21、活物質層12となる層を活物質層22とする。
図2及び図3に例示するように、二次電池用電極10は、長尺状芯体21の両面に活物質層22が形成された長尺状の電極前駆体20を所定の形状に切断して製造される。二次電池用電極10の製造工程は、長尺状芯体21の少なくとも一方の面に活物質層22を形成する第1工程と、連続発振レーザ(CWレーザ)を用いて、電極前駆体20を切断する第2工程とを含む。本実施形態では、第1の工程で長尺状芯体21の両面に活物質層22が形成される。第1工程では、活物質層22の構成材料を含む合材スラリーを調製し、当該スラリーを長尺状芯体21の両面に塗布し、塗膜を乾燥させて、活物質層22を形成する。
第1工程では、電極前駆体20の長手方向に沿って、芯体表面21sが露出した露出部23を形成する。露出部23は、長尺状芯体21の幅方向一端から略一定の幅で形成されることが好ましい。露出部23の幅は、例えば長尺状芯体21の幅の1/5以下である。露出部23は、長尺状芯体21の両面の全域に活物質層22を形成した後、活物質層22の一部を剥離除去して形成されてもよいが、好ましくは長尺状芯体21の一部に合材スラリーを塗布しないことにより形成される。長尺状芯体21は、例えば幅方向に2枚の二次電池用電極10を形成可能な幅を有する。この場合、電極前駆体20の幅方向両端部に露出部23が形成される。
第2工程では、レーザシステム30から出力されるレーザ光αを電極前駆体20に照射して、電極前駆体20を所定の形状に切断する。第2工程では、電極前駆体20とレーザシステム30の加工ヘッドとの相対位置を変化させながら、電極前駆体20に対してレーザ光αを照射する。電極前駆体20を固定した状態でレーザ光αを走査することも可能であるが、長尺状の電極前駆体20を加工する場合は、電極前駆体20を搬送しながら切断処理を行うことが好ましい。電極前駆体20を搬送しながら、レーザ光αを走査してもよい。
図2に例示するように、レーザシステム30は、レーザ発振器31と、ガルバノスキャナー33を内蔵する加工ヘッドとを備える。ガルバノスキャナー33を用いることで、加工ヘッド自体を固定した状態でレーザ光αを走査することができる。レーザ発振器31は、連続発振が可能な発振器である。レーザ発振器31の例としては、連続発振モードでレーザ光αを出力可能なYAGレーザ、CO2レーザ、Arレーザ、ファイバーレーザなどが挙げられる。好適な一例は、ファイバーレーザである。発振波長の好適な範囲の一例は、900nm~1200nmである。レーザシステム30では、レーザ発振器31とガルバノスキャナー33の間に、レーザ発振器31から出力されたレーザ光αを平行なビームとするコリメータ32が設けられている。
ガルバノスキャナー33は、レーザ発振器31側から順に、反射ミラー34、光学素子35、X軸ミラー36、Y軸ミラー37、及びFθレンズ38を有する。光学素子35には、例えば回折格子等が用いられる。コリメータ32を通過した連続波であるレーザ光αは、反射ミラー34で光学素子35側に曲げられ、光学素子35を通過して、X軸ミラー36、Y軸ミラー37に導かれる。X軸ミラー36及びY軸ミラー37を動かすことでレーザ光αを走査し、二次元平面内で照射スポットPの位置を変更することができる。X軸ミラー36及びY軸ミラー37で反射されたレーザ光αは、Fθレンズ38及び保護ガラス39を通って電極前駆体20に照射される。
図3に例示するように、第2工程では、連続発振レーザを用いて、電極前駆体20の活物質層22が設けられた部分を露出部23に沿って切断すると共に、略一定周期で切断方向を変えて露出部23を切断することによりリード部14となる凸部24を形成する。レーザ光αは、活物質層22が設けられた部分と露出部23の境界位置に照射することもできるが、この場合、照射スポットPの僅かなズレでリード部14以外の部分に芯体表面11sの露出部が形成される。リード部14以外の部分に形成される露出部は、正負極間の低抵抗な短絡を招くおそれがあるため、特に正極では当該露出部が形成されないように電極前駆体20を切断することが好ましい。このため、露出部23の近傍の活物質層22が設けられた部分にレーザ光αを照射して電極前駆体20を切断することが好ましい。
レーザ光αは、露出部23(電極前駆体20の長手方向)に沿って走査され、凸部24に対応する部分で露出部23側(電極前駆体20の幅方向)に走査される。活物質層22が設けられた部分と露出部23との境界位置においてもレーザ光αは連続的に照射されるため、活物質層22が設けられた部分の切断部C22と、露出部23の切断部C23とは、連続した1本の線状に形成される。略一定周期で切断方向を変えて露出部23を切断することで、電極前駆体20の長手方向に略等間隔で並ぶ複数の凸部24が形成される。そして、活物質層12が全体に形成された基部13と、付け根に活物質層12が形成されたリード部14とを有する二次電池用電極10が得られる。
第2工程では、連続発振レーザを用いて、電極前駆体20を電極サイズに切断してもよい。上述のように、長尺状芯体21が幅方向に2枚の二次電池用電極10が形成可能な幅を有する場合、凸部24を形成する切断工程後に、電極前駆体20の幅方向中央で長手方向に沿って電極前駆体20を切断する。幅方向中央で電極前駆体20を切断すると、1枚の二次電池用電極10に対応する幅に切断された電極前駆体20が得られるが、当該切断工程には、連続発振レーザを用いることが好ましい。詳しくは後述するが、1枚の二次電池用電極10に対応する幅にサイズ調整された電極前駆体20が、活物質層22の圧縮工程に供給されてもよい。
なお、電極前駆体20を切断予定部Xで切断して個々の電極サイズとした後、活物質層を圧縮してもよい。電極前駆体20を切断予定部Xで切断する工程は、連続発振レーザを用いて行われてもよく、カッター等を用いた従来の一般的な切断法を用いて行われてもよい。
図4は、電極前駆体20の切断部C22及びその近傍の断面を撮影した走査型電子顕微鏡(SEM)写真である。図3及び図4に示すように、連続発振されたレーザ光αを電極前駆体20の活物質層22が形成された部分に照射すると、切断部C22において、活物質層22の端面22e又はその近傍に突起25が形成される場合がある。この突起25は、レーザが照射されることにより溶融した活物質層22が両側に広がり、隣接する活物質層22上で凝固したものである。なお、突起25の活物質層22の上面からの突出高さは、10μm~100μmであることが好ましく、10μm~80μmであることがより好ましい。図3に示す例では、レーザ光αが先に入射する側の活物質層22の表面に突起25が形成されている。このような突起25は、正負極間の短絡の原因となるおそれがあるため、除去することが好ましい。例えば、活物質層22を圧縮することで、活物質層22に突起25を埋め込む、或いは活物質層22上から突起25を脱落させることができる。また、レーザ照射条件を制御して突起25の形成を抑制することもできる。
レーザ光αを電極前駆体20の活物質層22が形成された部分に照射すると、レーザ光αが先に入射する側の活物質層22の端面22eと芯体表面21sとがなす角度θ1は、例えば55°~85°とすることが好ましい。切断部C22では芯体表面21sが活物質層22に覆われて露出することがなく、切断部C22,C23のいずれも直線状の綺麗な切断部となる。角度θ1は、例えば反対側の活物質層22の表面と端面22eとがなす角度θ2と略同一とすることが好ましい。
レーザ照射条件は、長尺状芯体21及び活物質層22の材質、厚み、切断形状等に基づいて調整することが好ましいが、概ね、連続発振レーザ(レーザ発振器31)の出力は500W~5000W、レーザ光αのスポット径は5μm~100μmとすることが好ましい。また、連続発振レーザによる電極前駆体20の切断速度は、例えば500mm/s~8000mm/sとすることが好ましい。電極前駆体20が正極の前駆体である場合と、負極の前駆体である場合とで、照射条件を変更してもよい。一般的には、正極前駆体の方が切断し易い。
レーザ出力、スポット径、及び切断速度に関するより好適な範囲の一例は下記の通りである。
・レーザ出力は、1000W~3000Wであることが好ましい。
・スポット径は、10μm~100μmであることが好ましく、10μm~40μmであることが更に好ましい。
・切断速度は、1000mm/s~5000mm/sであることがより好ましい。
・レーザ出力は、1000W~3000Wであることが好ましい。
・スポット径は、10μm~100μmであることが好ましく、10μm~40μmであることが更に好ましい。
・切断速度は、1000mm/s~5000mm/sであることがより好ましい。
図5は、レーザ出力と切断速度との関係を示す図である。上述のように、レーザ出力は1000W~3000W、切断速度は1000mm/s~5000mm/sが好ましいが、レーザ出力と切断速度は、図5の三角形で示す関係とすることがより好ましい。即ち、レーザ出力:1000W、切断速度:1000mm/sの第1の点と、レーザ出力:3000W、切断速度:1000mm/sの第2の点と、レーザ出力:3000W、切断速度:5000mm/sの第3の点とを頂点とする三角形の中に入るように、レーザ出力と切断速度を調整することが好適である。
図5の三角形で示す範囲にレーザ出力と切断速度を調整することで、直線状の綺麗な切断部を形成し易くなり、さらに突起25の形成も抑えられる。また、1000mm/s以上の切断速度とすれば、良好な生産性も確保できる。なお、長尺状芯体21及び活物質層22の材質、厚み、切断形状等に応じて、さらに当該三角形の範囲内で照射条件を適宜変更することは好ましい。例えば、レーザ出力:3000W、切断速度:5000mm/sの第3の点に近い条件を適用した場合、他の2点に近い条件を適用した場合と比較して、高速な切断が可能であるが、切断部が粗くなる傾向が見られる。このため、切断形状が単純である場合に、第3の点に近い条件を適用してもよい。
二次電池用電極10の製造工程は、連続発振レーザにより切断された活物質層を圧縮する工程をさらに含むことが好ましい。活物質層の圧縮は、例えば電極前駆体20を両側から挟む圧延ローラを用いて行われる。活物質層の圧縮工程は、電極前駆体20の切断工程である第2工程の前に実施されてもよいが、好ましくは第2工程後に実施される。圧縮される前の電極前駆体20を連続発振レーザにより切断することで、直線状の綺麗な切断部を有する二次電池用電極を高速でより確実に作製することができる。また、圧縮工程を第2工程後に実施すると、連続発振レーザによる切断で突起25が形成されたとしても、突起25を押し潰して活物質層に埋め込む、或いは活物質層上から突起25を脱落させることができる。圧縮工程は、電極前駆体20を個々の電極サイズに切断した後に実施されてもよいが、生産性を考慮すると、例えば1枚の二次電池用電極10に対応する幅にサイズ調整された電極前駆体20の状態で行われることが好ましい。そして、圧縮工程の後、電極前駆体20を電極サイズに切断することが好ましい。
以上のように、連続発振レーザを用いて電極前駆体20を切断することにより、直線状の綺麗な切断部C22,C23等を高速で形成することができ、二次電池用電極10の生産性が大幅に向上する。
以下に二次電池用電極10を用いた二次電池100の構成について説明する。
図6に示すように、二次電池100は、複数枚の正極と複数枚の負極とがセパレータを介して交互に積層された電極体50が、電解液(不図示)とともに、電池ケース60内に収容されている。ここで、正極ないし負極として、二次電池用電極10を用いる。電池ケース60の開口部は、封口体61によって封口されている。正極端子62及び負極端子63が、それぞれ、樹脂部材64、65を介して、封口体61に固定されている。正極は正極リード部51及び正極集電部材52を介して正極端子62に電気的に接続されている。負極は負極リード部53及び負極集電部材54を介して負極端子63に電気的に接続されている。封口体61には、電解液を注液する注液孔が設けられ、この注液孔は、電解液を注液した後、封止部材66で封止される。また、封口体61には、電池ケース60の内部圧力が上昇したときに、圧力を開放するガス排出弁67が設けられている。電池ケース60が金属製である場合、電極体50を箱状又は袋状の絶縁シート55の内部に配置した状態で電池ケース60内に配置することが好ましい。
図6に示すように、二次電池100は、複数枚の正極と複数枚の負極とがセパレータを介して交互に積層された電極体50が、電解液(不図示)とともに、電池ケース60内に収容されている。ここで、正極ないし負極として、二次電池用電極10を用いる。電池ケース60の開口部は、封口体61によって封口されている。正極端子62及び負極端子63が、それぞれ、樹脂部材64、65を介して、封口体61に固定されている。正極は正極リード部51及び正極集電部材52を介して正極端子62に電気的に接続されている。負極は負極リード部53及び負極集電部材54を介して負極端子63に電気的に接続されている。封口体61には、電解液を注液する注液孔が設けられ、この注液孔は、電解液を注液した後、封止部材66で封止される。また、封口体61には、電池ケース60の内部圧力が上昇したときに、圧力を開放するガス排出弁67が設けられている。電池ケース60が金属製である場合、電極体50を箱状又は袋状の絶縁シート55の内部に配置した状態で電池ケース60内に配置することが好ましい。
なお、各正極から突出した正極リード部51は、湾曲した状態とし、正極集電部材52において、封口体61と略平行に配置される部分に接続されることが好ましい。また、各負極から突出した負極リード部53は、湾曲した状態とし、負極集電部材54において、封口体61と略平行に配置される部分に接続されることが好ましい。これにより、体積エネルギー密度のより高い二次電池となる。
また、連続発振レーザにより切断した端面を有する上述の方法で作製した正極ないし負極は、正極と負極の間に配置されるセパレータに接着されていることが好ましい。接着の方法としては、ポリプロピレンやポリエチレン等のポリオレフィン製等のセパレータの表面あるいは、電極の活物質層表面に接着層を設け、この接着層によりセパレータと活物質層を接着することが好ましい。接着としては圧着や熱溶着等が好ましい。接着層は特に限定されないが、セパレータよりも柔らかい層であることが好ましい。また、接着層として、樹脂製のものが好ましく、例えば、ポリフッ化ビニリデン、カルボキシメチルセルロース、ポリビニルアルコール等を用いることができる。
活物質層とセパレータを接着層により接着する場合は、接着層が突起痕15と接するようにすることが好ましい。これにより、二次電池を使用する際に突起痕15が活物質層から滑落することを防止できる。
なお、セパレータと活物質層が接着されると、活物質層内に電解液が浸透し難くなる可能性がある。しかしながら、上述のように、活物質層12の端面12eと芯体表面11sとがなす角度θ1が55°~85°となるようにすると、活物質層端面の面積が大きくなるため活物質層内への電解液が浸透し易くなる。
<その他>
リード部14において活物質層22と隣接する部分に、アルミナ、ジルコニア、チタニア等のセラミック粒子及び結着材からなる保護層を設けることもできる。また保護層に炭素材料等の導電材を含有させることもできる。
リード部14において活物質層22と隣接する部分に、アルミナ、ジルコニア、チタニア等のセラミック粒子及び結着材からなる保護層を設けることもできる。また保護層に炭素材料等の導電材を含有させることもできる。
長尺状の正極と長尺状の負極をセパレータを介して巻回した巻回型電極体に用いる、正極又は負極の製造方法として、本開示に係る二次電池用電極の製造方法を適用することが可能である。この場合、巻回型電極体の巻回軸が延びる方向における一方の端部側に、正極に設けられた複数の正極リード部と、負極に設けられた複数の負極リード部がそれぞれ配置されるようにすることが好ましい。これにより、より体積エネルギー密度の高い二次電池となる。なお、長尺状の正極に設けられた複数の正極リード部は等間隔ではなく、巻回型電極体において複数の正極リード部が積層されるように、間隔を変えて形成されることが好ましい。長尺状の負極に設けられた複数の負極リード部の形成位置についても同様である。
長尺状の正極が芯体の両面に活物質層が形成されたものであり、一方面側の活物質層(図1においては上方の活物質層)の活物質層の量が、他方面側の活物質層(図1においては下方の活物質層)の量よりも少ない場合、活物質層の量が少ない一方面側の活物質層が巻回型電極体の巻回中心側に配置されるようにすることが好ましい。巻回型電極体において正極に対して内側に位置する負極活物質層の量は、通常、外側に位置する負極活物質層の量よりも小さくなる。したがって、上述の構成であると、正極活物質層と負極活物質層の対向バランスがより好ましい状態となる。
10 二次電池用電極、11 芯体、11s 芯体表面、12 活物質層、12e,22e 端面、13 基部、14 リード部、15 突起痕、20 電極前駆体、21 長尺状芯体、21s 芯体表面、22 活物質層、22e 端面、23 露出部、24 凸部、25 突起、30 レーザシステム、31 レーザ発振器、32 コリメータ、33 ガルバノスキャナー、34 反射ミラー、35 光学素子、36 X軸ミラー、37 Y軸ミラー、38 Fθレンズ、39 保護ガラス、100 二次電池、C22,C23 切断部、α レーザ光、P 照射スポット、X 切断予定部
Claims (9)
- 長尺状芯体の少なくとも一方の面に活物質層を形成する第1工程と、
連続発振レーザを用いて、前記活物質層が形成された前記長尺状芯体である電極前駆体を所定の形状に切断する第2工程と、
を含む二次電池用電極の製造方法。 - 前記第1工程では、前記電極前駆体の長手方向に沿って、前記長尺状芯体の表面が露出した露出部を形成し、
前記第2工程では、前記連続発振レーザを用いて、前記電極前駆体の前記活物質層が設けられた部分を前記露出部に沿って切断すると共に、所定のタイミングで切断方向を変えて前記露出部を切断することにより電極リードとなる凸部を形成する、請求項1に記載の二次電池用電極の製造方法。 - 前記第2工程では、前記連続発振レーザを用いて、前記電極前駆体を電極サイズに切断する、請求項1又は2に記載の二次電池用電極の製造方法。
- 前記連続発振レーザにより切断された前記活物質層を圧縮する工程をさらに含む、請求項1~3のいずれか1項に記載の二次電池用電極の製造方法。
- 前記連続発振レーザの出力は、1000W~3000Wであり、
前記連続発振レーザから出力されたレーザ光のスポット径は、10μm~100μmであり、
前記連続発振レーザによる前記電極前駆体の切断速度は、1000mm/s~5000mm/sである、請求項1~4のいずれか1項に記載の二次電池用電極の製造方法。 - 前記第2工程では、連続発振レーザを用いて切断された部分において前記活物質層の端面と前記長尺状芯体の表面とがなす角度が、55°~85°であり、前記活物質層の端面又はその近傍には、突起が存在する、請求項1~5のいずれか1項に記載の二次電池用電極の製造方法。
- 請求項1~6のいずれか1項に記載の製造方法で作製された二次電池用電極を用いた二次電池の製造方法。
- 芯体と、
前記芯体の少なくとも一方の面に形成された活物質層と、
を備え、
前記活物質層の端面と前記芯体の表面とがなす角度が、55°~85°であり、
前記活物質層の端面又はその近傍には、突起痕が存在する、二次電池用電極。 - 芯体と、
前記芯体の少なくとも一方の面に形成された活物質層と、
を備え、
前記活物質層の端面と前記芯体の表面とがなす角度が、55°~85°であり、
前記活物質層の端面又はその近傍には、突起痕が存在する、二次電池用電極を備える二次電池。
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201780052883.2A CN109643786B (zh) | 2016-08-31 | 2017-08-29 | 二次电池用电极的制造方法和二次电池的制造方法 |
| US16/327,997 US11527744B2 (en) | 2016-08-31 | 2017-08-29 | Secondary-battery electrode and secondary-battery electrode manufacturing method, and secondary battery and method of manufacturing secondary battery |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2016170071A JP6931277B2 (ja) | 2016-08-31 | 2016-08-31 | 二次電池用電極の製造方法、及び二次電池の製造方法 |
| JP2016-170071 | 2016-08-31 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2018043443A1 true WO2018043443A1 (ja) | 2018-03-08 |
Family
ID=61300673
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2017/030827 Ceased WO2018043443A1 (ja) | 2016-08-31 | 2017-08-29 | 二次電池用電極及びその製造方法、並びに二次電池及びその製造方法 |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US11527744B2 (ja) |
| JP (1) | JP6931277B2 (ja) |
| CN (1) | CN109643786B (ja) |
| WO (1) | WO2018043443A1 (ja) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2020120096A1 (de) * | 2018-12-10 | 2020-06-18 | Robert Bosch Gmbh | Elektrodenstapel für eine galvanische zelle |
| WO2020137714A1 (ja) * | 2018-12-27 | 2020-07-02 | 三洋電機株式会社 | 二次電池 |
| CN114824490A (zh) * | 2021-01-29 | 2022-07-29 | 泰星能源解决方案有限公司 | 二次电池的制造方法以及二次电池 |
| JP2023053696A (ja) * | 2021-10-01 | 2023-04-13 | 古河電気工業株式会社 | 金属箔のレーザ切断方法 |
| US20230135592A1 (en) * | 2020-03-27 | 2023-05-04 | Sanyo Electric Co., Ltd. | Electrode plate for secondary battery, method for producing same, secondary battery, and method for producing same |
| JP2025531594A (ja) * | 2022-09-19 | 2025-09-22 | 珠海冠宇電池股分有限公司 | 電池極板、セルおよび電池 |
Families Citing this family (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20220021001A1 (en) * | 2018-12-27 | 2022-01-20 | Sanyo Electric Co., Ltd. | Electrode plate and secondary battery using same |
| WO2021058925A1 (fr) * | 2019-09-26 | 2021-04-01 | Saverglass | Procede de marquage a but decoratif d'articles en verre a haute temperature par laser |
| CN114514646B (zh) | 2019-09-30 | 2023-11-28 | 株式会社村田制作所 | 二次电池 |
| KR102803271B1 (ko) * | 2019-10-24 | 2025-05-07 | 주식회사 엘지에너지솔루션 | 레이저 식각을 이용한 전극 제조방법 및 이를 수행하는 전극 제조설비 |
| KR102873026B1 (ko) * | 2021-01-08 | 2025-10-17 | 주식회사 엘지에너지솔루션 | 전극의 절단방법 및 절단장치 |
| DE102021202644A1 (de) * | 2021-03-18 | 2022-09-22 | Volkswagen Aktiengesellschaft | Verfahren zur Herstellung einer Ableiterfolie für Batterien |
| CN115555852B (zh) * | 2021-06-30 | 2023-06-30 | 宁德时代新能源科技股份有限公司 | 极片成型方法及设备 |
| US20230034980A1 (en) * | 2021-07-29 | 2023-02-02 | Samsung Sdi Co., Ltd. | Cutting device and method for cutting an electrode foil for a secondary battery cell |
| CN115890095B (zh) * | 2021-09-30 | 2023-11-28 | 宁德时代新能源科技股份有限公司 | 一种电池组件装配方法、夹具及焊接设备 |
| JP7583704B2 (ja) | 2021-12-27 | 2024-11-14 | プライムプラネットエナジー&ソリューションズ株式会社 | 電極板の製造方法、二次電池の製造方法、電極板および二次電池 |
| US12330239B2 (en) * | 2022-02-09 | 2025-06-17 | Ford Global Technologies, Llc | Laser notching apparatus for cutting of electrode sheets |
| CN115064806B (zh) * | 2022-08-03 | 2025-08-22 | 武汉蔚能电池资产有限公司 | 一种激光切割装置以及电池回收系统 |
| JP2025537722A (ja) * | 2022-11-16 | 2025-11-20 | エルジー エナジー ソリューション リミテッド | 電極組立体および該電極組立体を含むバッテリー、並びに該バッテリーを含むバッテリーパックおよび自動車 |
| KR102792583B1 (ko) | 2024-03-28 | 2025-04-04 | 삼성에스디아이 주식회사 | 이차 전지용 전극 및 이의 제조 방법 |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH02170351A (ja) * | 1988-12-22 | 1990-07-02 | Matsushita Electric Ind Co Ltd | 円筒形電池とその製造法 |
| JP2006139919A (ja) * | 2004-11-10 | 2006-06-01 | Ngk Spark Plug Co Ltd | リチウムイオン二次電池およびその製造方法 |
| JP2010034009A (ja) * | 2008-07-31 | 2010-02-12 | Nec Tokin Corp | 積層型二次電池およびその製造方法 |
| JP2016033912A (ja) * | 2014-07-30 | 2016-03-10 | 三星エスディアイ株式会社Samsung SDI Co.,Ltd. | 二次電池およびその製造方法 |
| WO2016208679A1 (ja) * | 2015-06-24 | 2016-12-29 | 株式会社豊田自動織機 | 電極の製造方法、及び、電極 |
| WO2017110318A1 (ja) * | 2015-12-25 | 2017-06-29 | 株式会社豊田自動織機 | 蓄電装置、及び電極ユニットの製造方法 |
Family Cites Families (22)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2001176501A (ja) | 1999-12-16 | 2001-06-29 | Sony Corp | 非水電解質電池の製造方法 |
| JP5011632B2 (ja) * | 2004-06-29 | 2012-08-29 | Tdk株式会社 | スリッター装置及び電極の製造方法 |
| JP2007014993A (ja) | 2005-07-08 | 2007-01-25 | Toyota Motor Corp | レーザを用いたワーク切断方法とレーザ加工装置 |
| JP5008849B2 (ja) * | 2005-09-08 | 2012-08-22 | ソニーモバイルディスプレイ株式会社 | レーザ加工方法及び透明樹脂層を有する表示装置の製造方法 |
| KR20080058772A (ko) * | 2006-12-22 | 2008-06-26 | 에스케이에너지 주식회사 | 전지용 전극의 제조 방법 |
| JP2008194729A (ja) * | 2007-02-13 | 2008-08-28 | Fujitsu Ltd | 小型デバイスの製造方法、レーザ加工方法及びレーザ加工装置 |
| JP5225639B2 (ja) * | 2007-09-06 | 2013-07-03 | 浜松ホトニクス株式会社 | 半導体レーザ素子の製造方法 |
| JP4667495B2 (ja) * | 2007-11-05 | 2011-04-13 | パナソニック株式会社 | ローラ加工方法、およびローラ加工装置 |
| BR112012019544A2 (pt) * | 2010-02-04 | 2018-03-27 | Echelon Laser Systems Lp | metodo e sistema de corte com laser |
| JP2012221912A (ja) * | 2011-04-14 | 2012-11-12 | Nissan Motor Co Ltd | 電極製造方法および電極製造装置 |
| CN104870116A (zh) * | 2012-12-27 | 2015-08-26 | 村田机械株式会社 | 激光加工机的修边工具及其修边方法 |
| DE102013203810A1 (de) * | 2013-03-06 | 2014-09-11 | Thyssenkrupp System Engineering Gmbh | Verfahren und Vorrichtung zum Schneiden eines Elektrodenbands |
| US9048635B2 (en) * | 2013-03-13 | 2015-06-02 | Federal-Mogul Ignition Company | Spark plug with laser keyhole weld attaching ground electrode to shell |
| JP6064228B2 (ja) * | 2013-05-24 | 2017-01-25 | パナソニックIpマネジメント株式会社 | レーザ切断装置およびレーザ切断方法 |
| JP2015084279A (ja) * | 2013-10-25 | 2015-04-30 | トヨタ自動車株式会社 | 二次電池 |
| KR101680416B1 (ko) * | 2013-11-01 | 2016-12-12 | 주식회사 엘지화학 | 레이저를 이용한 양극 커팅 장치 |
| US10218029B2 (en) * | 2014-02-28 | 2019-02-26 | Nec Energy Devices, Ltd. | Electrode for secondary battery, secondary battery, and manufacturing method of the electrode and the secondary battery |
| CN104051705B (zh) * | 2014-07-07 | 2017-01-18 | 合肥国轩高科动力能源有限公司 | 一种高效多极耳卷绕式电池制片设备 |
| CN105322057B (zh) * | 2014-07-25 | 2020-03-20 | 晶元光电股份有限公司 | 发光元件及其制造方法 |
| JP6464687B2 (ja) * | 2014-11-13 | 2019-02-06 | 株式会社豊田自動織機 | 電極の製造方法及び電極のクリーニング装置 |
| JP6413697B2 (ja) * | 2014-11-25 | 2018-10-31 | 株式会社豊田自動織機 | 電極の製造方法および電極の製造装置 |
| WO2017119010A1 (ja) * | 2016-01-06 | 2017-07-13 | オー・エム・シー株式会社 | 原反の分割方法とその分割機構及び分割装置 |
-
2016
- 2016-08-31 JP JP2016170071A patent/JP6931277B2/ja active Active
-
2017
- 2017-08-29 WO PCT/JP2017/030827 patent/WO2018043443A1/ja not_active Ceased
- 2017-08-29 US US16/327,997 patent/US11527744B2/en active Active
- 2017-08-29 CN CN201780052883.2A patent/CN109643786B/zh active Active
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH02170351A (ja) * | 1988-12-22 | 1990-07-02 | Matsushita Electric Ind Co Ltd | 円筒形電池とその製造法 |
| JP2006139919A (ja) * | 2004-11-10 | 2006-06-01 | Ngk Spark Plug Co Ltd | リチウムイオン二次電池およびその製造方法 |
| JP2010034009A (ja) * | 2008-07-31 | 2010-02-12 | Nec Tokin Corp | 積層型二次電池およびその製造方法 |
| JP2016033912A (ja) * | 2014-07-30 | 2016-03-10 | 三星エスディアイ株式会社Samsung SDI Co.,Ltd. | 二次電池およびその製造方法 |
| WO2016208679A1 (ja) * | 2015-06-24 | 2016-12-29 | 株式会社豊田自動織機 | 電極の製造方法、及び、電極 |
| WO2017110318A1 (ja) * | 2015-12-25 | 2017-06-29 | 株式会社豊田自動織機 | 蓄電装置、及び電極ユニットの製造方法 |
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2020120096A1 (de) * | 2018-12-10 | 2020-06-18 | Robert Bosch Gmbh | Elektrodenstapel für eine galvanische zelle |
| WO2020137714A1 (ja) * | 2018-12-27 | 2020-07-02 | 三洋電機株式会社 | 二次電池 |
| JPWO2020137714A1 (ja) * | 2018-12-27 | 2021-11-11 | 三洋電機株式会社 | 二次電池 |
| JP7353302B2 (ja) | 2018-12-27 | 2023-09-29 | 三洋電機株式会社 | 二次電池 |
| US12438242B2 (en) | 2018-12-27 | 2025-10-07 | Sanyo Electric Co., Ltd. | Secondary battery |
| US20230135592A1 (en) * | 2020-03-27 | 2023-05-04 | Sanyo Electric Co., Ltd. | Electrode plate for secondary battery, method for producing same, secondary battery, and method for producing same |
| CN114824490A (zh) * | 2021-01-29 | 2022-07-29 | 泰星能源解决方案有限公司 | 二次电池的制造方法以及二次电池 |
| JP2023053696A (ja) * | 2021-10-01 | 2023-04-13 | 古河電気工業株式会社 | 金属箔のレーザ切断方法 |
| JP7704641B2 (ja) | 2021-10-01 | 2025-07-08 | 古河電気工業株式会社 | 金属箔のレーザ切断方法 |
| JP2025531594A (ja) * | 2022-09-19 | 2025-09-22 | 珠海冠宇電池股分有限公司 | 電池極板、セルおよび電池 |
Also Published As
| Publication number | Publication date |
|---|---|
| US11527744B2 (en) | 2022-12-13 |
| JP2018037308A (ja) | 2018-03-08 |
| CN109643786B (zh) | 2021-11-16 |
| US20190198853A1 (en) | 2019-06-27 |
| JP6931277B2 (ja) | 2021-09-01 |
| CN109643786A (zh) | 2019-04-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6931277B2 (ja) | 二次電池用電極の製造方法、及び二次電池の製造方法 | |
| CN109690829B (zh) | 二次电池用电极和二次电池 | |
| TWI397203B (zh) | Laminated type secondary battery and manufacturing method thereof | |
| US10283815B2 (en) | Production method of laminate for a battery | |
| US20110195288A1 (en) | Sealed battery and method for fabricating the same | |
| CN109834393B (zh) | 电极片制造装置和蓄电装置的制造方法 | |
| CN111279523B (zh) | 二次电池用的电极以及使用了该电极的二次电池 | |
| US11557794B2 (en) | Solid-state battery and method of manufacture thereof | |
| JP2009259697A (ja) | 電池およびその製造方法 | |
| CN113039662B (zh) | 二次电池用的电极板和使用了该电极板的二次电池 | |
| US12548860B2 (en) | Electrode plate for secondary cell, and secondary cell using same | |
| JP6727990B2 (ja) | 二次電池用電極の製造方法、及び二次電池の製造方法 | |
| WO2020137714A1 (ja) | 二次電池 | |
| US20240178460A1 (en) | Positive electrode for lithium-ion battery, battery core, and lithium-ion battery | |
| JP3178500U (ja) | リード部材 | |
| CN115398665B (zh) | 二次电池用电极板及其制造方法、以及二次电池及其制造方法 | |
| JP2021034242A (ja) | 全固体電池の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 17846448 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 17846448 Country of ref document: EP Kind code of ref document: A1 |