EP1954418B1 - Verfahren und vorrichtung zur reinigung bzw. entzunderung von dünnbrammen und bändern in warmbandstrassen, bandbehandlungsanlagen oder dergleichen - Google Patents
Verfahren und vorrichtung zur reinigung bzw. entzunderung von dünnbrammen und bändern in warmbandstrassen, bandbehandlungsanlagen oder dergleichen Download PDFInfo
- Publication number
- EP1954418B1 EP1954418B1 EP06818606A EP06818606A EP1954418B1 EP 1954418 B1 EP1954418 B1 EP 1954418B1 EP 06818606 A EP06818606 A EP 06818606A EP 06818606 A EP06818606 A EP 06818606A EP 1954418 B1 EP1954418 B1 EP 1954418B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- strips
- strip
- descaling
- thin slabs
- cryogens
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 238000000034 method Methods 0.000 title claims abstract description 18
- 238000009434 installation Methods 0.000 title abstract description 6
- 238000007670 refining Methods 0.000 title 1
- 239000007788 liquid Substances 0.000 claims abstract description 18
- 238000005096 rolling process Methods 0.000 claims abstract description 12
- 150000001875 compounds Chemical class 0.000 claims abstract 3
- 239000007921 spray Substances 0.000 claims description 10
- 239000002245 particle Substances 0.000 claims description 5
- 238000005507 spraying Methods 0.000 claims 2
- 238000012216 screening Methods 0.000 claims 1
- 238000004140 cleaning Methods 0.000 abstract description 14
- QVGXLLKOCUKJST-UHFFFAOYSA-N atomic oxygen Chemical compound [O] QVGXLLKOCUKJST-UHFFFAOYSA-N 0.000 abstract 1
- 229910052760 oxygen Inorganic materials 0.000 abstract 1
- 239000001301 oxygen Substances 0.000 abstract 1
- 239000007789 gas Substances 0.000 description 19
- 230000000694 effects Effects 0.000 description 10
- 239000011261 inert gas Substances 0.000 description 5
- 238000005554 pickling Methods 0.000 description 5
- 229910000831 Steel Inorganic materials 0.000 description 4
- 239000002253 acid Substances 0.000 description 4
- 238000005098 hot rolling Methods 0.000 description 4
- 239000010959 steel Substances 0.000 description 4
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 4
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 description 3
- 238000005097 cold rolling Methods 0.000 description 3
- CURLTUGMZLYLDI-UHFFFAOYSA-N Carbon dioxide Chemical compound O=C=O CURLTUGMZLYLDI-UHFFFAOYSA-N 0.000 description 2
- VEXZGXHMUGYJMC-UHFFFAOYSA-N Hydrochloric acid Chemical compound Cl VEXZGXHMUGYJMC-UHFFFAOYSA-N 0.000 description 2
- QAOWNCQODCNURD-UHFFFAOYSA-N Sulfuric acid Chemical compound OS(O)(=O)=O QAOWNCQODCNURD-UHFFFAOYSA-N 0.000 description 2
- 230000001154 acute effect Effects 0.000 description 2
- 238000005266 casting Methods 0.000 description 2
- 238000001816 cooling Methods 0.000 description 2
- 238000000605 extraction Methods 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 150000007513 acids Chemical class 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000001569 carbon dioxide Substances 0.000 description 1
- 229910002092 carbon dioxide Inorganic materials 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 238000009749 continuous casting Methods 0.000 description 1
- 239000000110 cooling liquid Substances 0.000 description 1
- 238000009826 distribution Methods 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- 230000008030 elimination Effects 0.000 description 1
- 238000003379 elimination reaction Methods 0.000 description 1
- 238000005265 energy consumption Methods 0.000 description 1
- 238000001704 evaporation Methods 0.000 description 1
- 230000008020 evaporation Effects 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 239000002184 metal Substances 0.000 description 1
- 229910052757 nitrogen Inorganic materials 0.000 description 1
- JCXJVPUVTGWSNB-UHFFFAOYSA-N nitrogen dioxide Inorganic materials O=[N]=O JCXJVPUVTGWSNB-UHFFFAOYSA-N 0.000 description 1
- 231100000252 nontoxic Toxicity 0.000 description 1
- 230000003000 nontoxic effect Effects 0.000 description 1
- 230000003647 oxidation Effects 0.000 description 1
- 238000007254 oxidation reaction Methods 0.000 description 1
- 238000009420 retrofitting Methods 0.000 description 1
- 230000000630 rising effect Effects 0.000 description 1
- 238000004904 shortening Methods 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 239000013589 supplement Substances 0.000 description 1
- 238000004381 surface treatment Methods 0.000 description 1
- 239000002341 toxic gas Substances 0.000 description 1
- 230000009466 transformation Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B08—CLEANING
- B08B—CLEANING IN GENERAL; PREVENTION OF FOULING IN GENERAL
- B08B7/00—Cleaning by methods not provided for in a single other subclass or a single group in this subclass
- B08B7/0021—Cleaning by methods not provided for in a single other subclass or a single group in this subclass by liquid gases or supercritical fluids
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B08—CLEANING
- B08B—CLEANING IN GENERAL; PREVENTION OF FOULING IN GENERAL
- B08B3/00—Cleaning by methods involving the use or presence of liquid or steam
- B08B3/02—Cleaning by the force of jets or sprays
- B08B3/022—Cleaning travelling work
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/02—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for lubricating, cooling, or cleaning
- B21B45/0269—Cleaning
- B21B45/0275—Cleaning devices
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/04—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for de-scaling, e.g. by brushing
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23G—CLEANING OR DE-GREASING OF METALLIC MATERIAL BY CHEMICAL METHODS OTHER THAN ELECTROLYSIS
- C23G5/00—Cleaning or de-greasing metallic material by other methods; Apparatus for cleaning or de-greasing metallic material with organic solvents
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/02—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for lubricating, cooling, or cleaning
- B21B45/0269—Cleaning
- B21B45/0272—Cleaning compositions
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/02—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for lubricating, cooling, or cleaning
- B21B45/0269—Cleaning
- B21B45/0275—Cleaning devices
- B21B45/0287—Cleaning devices removing solid particles, e.g. dust, rust
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/04—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for de-scaling, e.g. by brushing
- B21B45/08—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for de-scaling, e.g. by brushing hydraulically
Definitions
- the invention relates to a method for cleaning or descaling of thin slabs and strips in hot strip mills, strip processing plants or the like and to an apparatus for carrying out the method.
- the slab or strip is subject to continuous scaling during transport through the kiln and rolling train.
- This scale is usually removed with the help of scale scrubbers before a rolling is performed.
- water is injected at high pressure (about 200 ... 380 bar) onto the warm surface.
- high pressure about 200 ... 380 bar
- this cooling effect has a particularly disturbing effect due to the low transport speeds.
- the scale In the case of strip processing plants, the scale is generally removed with the aid of pickling lines before a rolling is carried out. In this case, the band is pulled through a warm acid bath (hydrochloric acid, sulfuric acid, mixed acids, etc.). Due to the chemical reactions, the desired cleaning process occurs. However, this process is expensive and not necessarily environmentally friendly because of the acid bath used.
- a warm acid bath hydrochloric acid, sulfuric acid, mixed acids, etc.
- the publication US 5,758,530 discloses a rolling line with at least one pair of opposed rollers between which a material to be rolled is reduced in thickness.
- Descaling devices are provided above and / or below the metal strip, each of the descaling devices comprising spray nozzles for a liquid, for a gas or for plasma.
- the spray nozzles are each formed as a pair of nozzles, wherein a first spray nozzle of the pair is arranged so that it sprays the spray medium at an acute angle in the transport direction of the tape on the surface and wherein a second nozzle of the pair is arranged so that it under the spray medium sprays an acute angle in the transport direction of the tape.
- the two nozzles are also arranged so that the two of them rising spray meet together.
- the publication DE 101 60 902 A1 discloses an apparatus for the cleaning of objects by means of a high-pressure jet of a cryogenic liquid gas. It contains a storage tank for the cryogenic liquid gas, a high-pressure pump and at least one cleaning nozzle.
- the international patent application WO 01/32335 A1 discloses a method for producing a steel strand on a continuous casting plant. According to the method, the steel strand is first passed through a device having an atmosphere led, which prevents oxidation of the surface of the steel strand and consequently the formation of scale. Subsequently, the steel strand is rolled and descaled. Finally, the rolled and descaled strand or the rolled and descaled strip are wound on a coiler into a coil.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Metal Rolling (AREA)
- Cleaning And De-Greasing Of Metallic Materials By Chemical Methods (AREA)
- Cleaning In General (AREA)
- Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
- Cleaning By Liquid Or Steam (AREA)
Description
- Die Erfindung betrifft ein Verfahren zur Reinigung bzw. Entzunderung von Dünnbrammen und Bändern in Warmbandstraßen, Bandbehandlungsanlagen oder dergleichen sowie eine Vorrichtung zur Durchführung des Verfahrens.
- Beim Warmwalzprozess in Warmbandstraßen unterliegt die Bramme bzw. das Band beim Transport durch Ofen und Walzstraße einer ständigen Verzunderung. Dieser Zunder wird in der Regel mit Hilfe von Zunderwäschern entfernt, bevor eine Walzung durchgeführt wird. Hierbei wird Wasser mit hohem Druck (ca. 200 ... 380 bar) auf die warme Oberfläche gespritzt. Infolge der Beaufschlagung mit Wasser kommt es neben dem erwünschten Reinigungsprozess zu einer nicht unwesentlichen Abkühlung des Bandes. Bei Walzanlagen, bei denen die Gießmaschine mit der Walzstraße direkt verbunden ist, d. h. mit Gießgeschwindigkeit gewalzt wird, wirkt sich dieser Kühleffekt infolge der niedrigen Transportgeschwindigkeiten besonders störend aus.
- Bei Bandbehandlungsanlagen wird der Zunder in der Regel mit Hilfe von Beizlinien entfernt, bevor eine Walzung durchgeführt wird. Hierbei wird das Band durch ein warmes Säurebad (Salzsäure, Schwefelsäure, Mischsäuren usw.) gezogen. Infolge der chemischen Reaktionen kommt es zu dem erwünschten Reinigungsprozess. Dieser Prozess ist jedoch aufwendig und wegen des verwendeten Säurebades nicht unbedingt umweltfreundlich.
- In dem Dokument
DE 1 99 53 230 C2 ist zwar ein Kaltwalzverfahren beschrieben, bei dem in den Bereich des Walzspalts anstatt Kühlflüssigkeit Inertgas geblasen wird, welches eine unterhalb von Raumtemperatur liegende Inertgastemperatur hat, die geringer ist als die Walzguttemperatur im Walzspalt und aus derWO02/087803 - Die Druckschrift
US 5,758,530 offenbart eine Walzlinie mit mindestens einem Paar von gegenüberliegenden Walzen, zwischen denen ein zu walzendes Gut dickenreduziert wird. Oberhalb und/oder unterhalb des Metallbandes sind Entzunderungseinrichtungen vorgesehen, wobei jede der Entzunderungseinrichtungen Sprühdüsen für eine Flüssigkeit, für ein Gas oder für Plasma umfasst. Die Sprühdüsen sind jeweils als Düsenpaar ausgebildet, wobei eine erste Sprühdüse des Paares so angeordnet ist, dass sie das Sprühmedium unter einem spitzen Winkel in Transportrichtung des Bandes auf dessen Oberfläche sprüht und wobei eine zweite Düse des Paares so angeordnet ist, dass sie das Sprühmedium unter einem spitzen Winkel in Transportrichtung des Bandes sprüht. Die beiden Düsen sind darüber hinaus so angeordnet, dass die beiden von ihnen aufgehenden Sprühstrahlen zusammen treffen. - Die Druckschrift
DE 101 60 902 A1 offenbart eine Vorrichtung für das Reinigen von Objekten mit Hilfe eines Hochdruckstrahles eines tiefkaltflüssigen Gases. Sie enthält einen Speicherbehälter für das tiefkalte flüssige Gas, eine Hochdruckpumpe und mindestens einer Reinigungsdüse. - Die internationale Patentanmeldung
WO 01/32335 A1 - Es werden also aufgabegemäß Alternativen gesucht, beim Warmwalzen den Temperaturverlust beim Entzunderungsprozess zu minimieren und den Reinigungseffekt zu verbessern sowie bei Bandbehandlungsanlagen die Reinigung des Bandes zu verbessern.
- Als vorteilhafte Lösung der Aufgabe erweist sich die Verwendung von Kyrogenen für das Reinigungs- bzw. Entzunderungsverfahren von Brammen oder Bändern. Hierbei handelt es sich um flüssige Gase, wie z.B. flüssiger Stickstoff oder Kohlendioxid. Es können die Gase in Reinform oder unter Verwendung mit Druckluft oder mit einem anderen geeigneten Trägermedium eingesetzt werden. Das flüssige Gas wird analog wie das Wasser des Zunderwäschers auf die Brammen- oder Bandoberfläche gespritzt bzw. auf das zu entzundernde Band. Da es sich jedoch um flüssiges Gas handelt, verflüchtigt es sich nach dem Auftreffen auf der Oberfläche und bewirkt so nur eine minimale Temperaturreduktion. Das ungiftige Gas mit den Staub- bzw. Zunderpartikel wird gegebenenfalls anschließend abgesaugt. Die Reinigungswirkung oder Entzunderungswirkung basiert auf drei Effekten:
- Thermischer Effekt
Dabei entstehen Mikrorisse in der Zunderschicht sowie zwischen Zunder und Band. - Kinetischer Effekt
Die flüssigen Partikel treffen auf die Oberfläche auf und dringen in die erzeugten Spalte ein. - Phasenumwandlung
Die schlagartige Volumenvergrößerung des flüssigen Gases sprengt die Zunderschicht bzw. Schmutzschicht ab. - Bei diesem Prozess ergeben sich beim Warmwalzen in einer Warmbandstraße folgende Vorteile:
- Entfernen des Zunders
- Geringer Temperaturverlust bei der Reinigung der Oberfläche
- Der geringere Temperaturverlust kann genutzt werden:
- * zur Einsparung von Heizenergie, indem die Ofentemperatur niedriger gewählt wird.
- * Verminderung der Fertigbanddicke bei ausreichender Endwalztemperatur.
- * Erweiterung der Anlagenkonfiguration (gekoppelter Gieß-Walz-Prozess).
- * Wegfall des konventionellen Zunderwäschers mit entsprechender Druckwasserversorgung und hierdurch weitere Energieeinsparung.
- * Weniger Temperatursteifigkeiten über der Bandbreite wird erwartet.
- * Zusätzlich zu der Entzunderungswirkung ist neben der Beaufschlagungsstelle der Bereich des Bandes mit Inertgas umgeben (das Gas verteilt sich). Dort wird zusätzlich die erneute Verzunderung unterdrückt.
- Bei diesem Prozess ergeben sich für Bandanlagen folgende Vorteile:
- Entfernen des Zunders
- Geringerer Säureverbrauch in der Beize
- Geringerer Energieverbrauch der Beize
- Verkürzung des Beizbehälters, bzw. Einsparung einer, oder mehrerer Beizstufen
- Effizienzerhöhung bei alternativen Entzunderungsverfahren
- Produktionserhöhung vorhandener Beizlinien
- Stickstoffentzunderung als Ersatz für einen Steckrichter (Zunderbrecher). D. h. Einsparung des Streckrichters (Zunderbrecher).
- In den
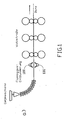
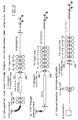
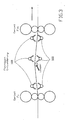
Figuren 1 bis 6 sind mögliche Einbauorte für die Entzunderungseinrichtung mit flüssigem Gas in einer Warmbandstraße aufgeführt: - Figur 1
- stellt die Anordnung hinter einer Gießanlage vor einer Walzstraße oder einem Ofen dar. Hier ist die Transportgeschwindigkeit beson- ders niedrig. Eine konventionelle Entzunderung ist hier schwierig zu realisieren.
- Figur 2
- zeigt mögliche Einbauorte vor einer Fertigstraße.
- In Figur 3
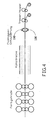
- sind Anwendungen zwischen zwei Gerüsten einer Fertigstraße zu sehen. Durch Entfernen der dünnen Zunderschicht wird das Einwal- zen des neu gebildeten Sekundärzunders unterdrückt. Um die Zun- derdicke am Fertigband (Coil) zu vermindern, mit dem Ziel die Beiz- geschwindigkeit zu steigern, ist eine Flüssiggas-Enzunderung kurz vor dem Treiber/Haspel vorgesehen, was
- Figur 4
- zeigt.
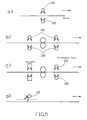
- Figur 5
- zeigt, dass die Flüssiggasreinigung als Einzeleinrichtung mit einem oder mehreren Spritzbalken ausgeführt sein kann oder in Kombinati- on mit einer konventionellen Entzunderung bzw. Niederdruck- Bandreinigung betrieben werden kann.
- Figur 6
- stell dar, wie eine Absaugung des Gases bzw. der Zunderpartikel ausgeführt sein kann. Weiterhin sieht man in
Figur 6 die ausgeführte Abschirmung der Verteilerleitung vor dem warmen Band. Weiterhin ist zu beachten, dass die Düse möglichst dicht vor dem Band positi- oniert ist, damit die volle Wirkung entsteht und die Flüssigkeit vor dem Verdampfen auf die Oberfläche auftritt. - Mögliche Einbauorte für die Entzunderungseinrichtung mit flüssigem Gas in einer Bandanlage sind:
- 1. Eine Anordnung als Ergänzung eines Streckrichters. D.h. die Düsen werden in, bzw. direkt an den Streckrichter angebaut. Dieser Einbauort bietet sich auch für Nachrüstungen an, weil dort bereits Absauganlagen Installiert sind.
- 2. Die Entzunderungseinrichtung mit flüssigem Gas als "stand alone" Anwendung eventuell als Ersatz für den Streckrichter.
Claims (2)
- Verfahren zur Entzunderung von Dünnbrammen in einer Warmbandstraße oder von Bändern in einer Bandbehandlungsanlage durch Aufspritzen eines flüssigen Gases auf die zu entzundernden Oberflächen der Dünnbrammen oder Bänder,
dadurch gekennzeichnet,
dass es sich bei dem flüssigen, tiefkalten Gas um eine Verbindung von Kyrogenen mit einem Trägermedium wie Druckluft handelt; und dass das verflüchtigte Kyrogen ggf. zusammen mit dem Trägermedium und Zunderpartikeln von den Dünnbrammen bzw. den Bändern abgesaugt wird. - Vorrichtung zur Durchführung des Verfahrens nach Anspruch 1, mit einem oder mehreren Spritzbalken oberhalb bzw. unterhalb der Dünnbrammen bzw. der Bänder zum Aufspritzen des flüssigen Gases auf die Ober- oder Unterseite der Dünnbrammen oder der Bänder;
dadurch gekennzeichnet,
dass es sich bei dem flüssigen Gas um eine Verbindung von Kyrogenen mit einem Trägermedium wie Druckluft handelt; und
dass die Spritzbalken von einer Abschirmhaube mit einer Absaugung umgeben sind zum Absaugen des Gases und der Zunderpartikel.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102005057679 | 2005-12-01 | ||
| DE102006019544A DE102006019544A1 (de) | 2005-12-01 | 2006-04-27 | Verfahren und Vorrichtung zur Entzunderung von Dünnbrammen und Bändern in Warmbandstraßen, Bandbehandlungsanlagen oder dergleichen |
| PCT/EP2006/011021 WO2007062749A1 (de) | 2005-12-01 | 2006-11-17 | Verfahren und vorrichtung zur reinigung bzw. entzunderung von dünnbrammen und bändern in warmbandstrassen, bandbehandlungsanlagen oder dergleichen |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1954418A1 EP1954418A1 (de) | 2008-08-13 |
| EP1954418B1 true EP1954418B1 (de) | 2011-01-12 |
Family
ID=37546797
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP06818606A Not-in-force EP1954418B1 (de) | 2005-12-01 | 2006-11-17 | Verfahren und vorrichtung zur reinigung bzw. entzunderung von dünnbrammen und bändern in warmbandstrassen, bandbehandlungsanlagen oder dergleichen |
Country Status (10)
| Country | Link |
|---|---|
| US (1) | US20090014037A1 (de) |
| EP (1) | EP1954418B1 (de) |
| JP (1) | JP2009511277A (de) |
| CN (1) | CN101253012B (de) |
| AT (1) | ATE494969T1 (de) |
| BR (1) | BRPI0619123A2 (de) |
| CA (1) | CA2626426A1 (de) |
| DE (2) | DE102006019544A1 (de) |
| RU (1) | RU2388559C2 (de) |
| WO (1) | WO2007062749A1 (de) |
Families Citing this family (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20100132747A1 (en) * | 2008-12-01 | 2010-06-03 | Ken Smith | Thermal De-Scaling Surfaces With Cryogenic Liquids And Gases |
| DE102009035161A1 (de) | 2009-07-29 | 2011-02-10 | Sms Siemag Ag | Verfahren und Vorrichtung zur Entzunderung oder Reinigung von metallischen Oberflächen, unter anderem Bänder (oder Brammen) im Durchlauf |
| EP2489446A1 (de) | 2011-02-17 | 2012-08-22 | Linde Aktiengesellschaft | Düsenkopf |
| CN103433310B (zh) * | 2013-09-18 | 2015-07-15 | 河南理工大学 | 一种热轧金属的除鳞方法 |
| CN103481201A (zh) * | 2013-10-16 | 2014-01-01 | 山西太钢不锈钢股份有限公司 | 金属板带表面连续除鳞的装置与方法 |
| DE102014101159B4 (de) * | 2014-01-30 | 2016-12-01 | Thyssenkrupp Steel Europe Ag | Verfahren zur Oberflächenbehandlung von Werkstücken |
| DE102014214027A1 (de) * | 2014-07-18 | 2016-02-18 | Bayerische Motoren Werke Aktiengesellschaft | Formwerkzeug zur Herstellung von warmumgeformten Bauteilen |
| CN107188291B (zh) * | 2017-06-05 | 2020-08-04 | 华中师范大学 | 一种液氮低温处理商业铁粉增强其还原去除污染物能力的方法 |
| IT201700118889A1 (it) * | 2017-10-20 | 2019-04-20 | Luca Patauner | Utilizzo dell'ossigeno liquido per la preparazione di superfici ad uso dei trattamenti di finitura superficiale |
| GB201808639D0 (en) | 2018-05-25 | 2018-07-11 | Additive Manufacturing Tech Ltd | Additive manufacturing |
| DE102020201560A1 (de) | 2020-02-07 | 2021-08-12 | Thyssenkrupp Steel Europe Ag | Verfahren zur Unterdrückung von Zunderbildung auf der Oberfläche eines metallischen Walzgutes |
| KR102866731B1 (ko) * | 2022-12-09 | 2025-09-29 | 김두원 | 스케일 제거장치와 스케일 제거방법 |
| CN116833252B (zh) * | 2023-09-01 | 2023-11-17 | 太原科技大学 | 一种适用于金属极薄带材生产的除渣润滑一体机 |
Family Cites Families (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4491484A (en) * | 1981-11-24 | 1985-01-01 | Mobile Companies, Inc. | Cryogenic cleaning process |
| US4806171A (en) * | 1987-04-22 | 1989-02-21 | The Boc Group, Inc. | Apparatus and method for removing minute particles from a substrate |
| US5395454A (en) * | 1993-12-09 | 1995-03-07 | Liquid Air Corporation | Method of cleaning elongated objects |
| EP0719602B1 (de) * | 1994-07-18 | 2001-11-21 | Kawasaki Steel Corporation | Verfahren und vorrichtung zum reinigen von stahlblech |
| US5579209A (en) * | 1994-10-19 | 1996-11-26 | Whirlpool Corporation | Remote control housing with functional attributes for a room air conditioner |
| US5616067A (en) * | 1996-01-16 | 1997-04-01 | Ford Motor Company | CO2 nozzle and method for cleaning pressure-sensitive surfaces |
| CN1087665C (zh) * | 1996-03-04 | 2002-07-17 | 三菱重工业株式会社 | 热轧设备 |
| CN2267106Y (zh) * | 1996-04-23 | 1997-11-12 | 鞍山钢铁集团公司 | 引射抽吸冷轧带钢表面乳化液装置 |
| AUPQ385099A0 (en) * | 1999-11-03 | 1999-11-25 | Bhp Steel (Jla) Pty Limited | Production of thin steel strip |
| DE19953230C2 (de) * | 1999-11-04 | 2003-08-28 | C D Waelzholz Produktionsgmbh | Kaltwalzverfahren |
| US6675622B2 (en) * | 2001-05-01 | 2004-01-13 | Air Products And Chemicals, Inc. | Process and roll stand for cold rolling of a metal strip |
| DE10160902A1 (de) * | 2001-12-12 | 2003-07-03 | Messer Griesheim Gmbh | Reinigen von Objekten mit Flüssiggas |
| DE10332693A1 (de) * | 2003-07-18 | 2005-02-10 | Sms Demag Ag | Verfahren und Vorrichtung zum Entzundern und/oder reinigen eines Metallstranges |
| CN2644038Y (zh) * | 2003-08-27 | 2004-09-29 | 攀枝花新钢钒股份有限公司热轧板厂 | 高压水除鳞挡水装置 |
| DE102004040375A1 (de) * | 2004-06-09 | 2005-12-29 | Sms Demag Ag | Verfahren und Walzgerüst zum Kaltwalzen von metallischem Walzgut, insbesondere von Walzband, mit Düsen für gasförmige oder flüssige Behandlungsmedien |
-
2006
- 2006-04-27 DE DE102006019544A patent/DE102006019544A1/de not_active Withdrawn
- 2006-11-17 DE DE502006008740T patent/DE502006008740D1/de active Active
- 2006-11-17 JP JP2008535991A patent/JP2009511277A/ja active Pending
- 2006-11-17 WO PCT/EP2006/011021 patent/WO2007062749A1/de not_active Ceased
- 2006-11-17 US US12/085,820 patent/US20090014037A1/en not_active Abandoned
- 2006-11-17 RU RU2008111501/02A patent/RU2388559C2/ru not_active IP Right Cessation
- 2006-11-17 AT AT06818606T patent/ATE494969T1/de active
- 2006-11-17 EP EP06818606A patent/EP1954418B1/de not_active Not-in-force
- 2006-11-17 CA CA002626426A patent/CA2626426A1/en not_active Abandoned
- 2006-11-17 BR BRPI0619123-1A patent/BRPI0619123A2/pt not_active IP Right Cessation
- 2006-11-17 CN CN200680032079XA patent/CN101253012B/zh not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| DE102006019544A1 (de) | 2007-06-06 |
| RU2008111501A (ru) | 2009-10-10 |
| CA2626426A1 (en) | 2007-06-07 |
| BRPI0619123A2 (pt) | 2011-09-13 |
| DE502006008740D1 (de) | 2011-02-24 |
| RU2388559C2 (ru) | 2010-05-10 |
| CN101253012B (zh) | 2010-12-29 |
| EP1954418A1 (de) | 2008-08-13 |
| US20090014037A1 (en) | 2009-01-15 |
| JP2009511277A (ja) | 2009-03-19 |
| CN101253012A (zh) | 2008-08-27 |
| ATE494969T1 (de) | 2011-01-15 |
| WO2007062749A1 (de) | 2007-06-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| KR100496607B1 (ko) | 열연코일의 제조방법 및 그 장치 | |
| EP1814678B2 (de) | Verfahren und vorrichtung zum entzundern eines metallbandes | |
| DE69919031T2 (de) | Verfahren zur herstellung rostfreier stahlbänder und integrierter walzstrasse | |
| CN205165369U (zh) | 热轧带钢表面氧化铁皮清理装置 | |
| DE60014145T2 (de) | Verfahren zum herstellen von kohlenstoffstahlbändern, insbesondere für verpackungsmaterial, und so hergestellte bändern | |
| DE69930303T2 (de) | Verfahren zur herstellung von bändern und walzstrasse | |
| EP0695808A1 (de) | Verfahren zum Herstellen von kaltgewalzten Stahlbändern aus nichtrostendem Stahl und Metallbändern, insbesondere aus Titanlegierungen | |
| EP1954418A1 (de) | Verfahren und vorrichtung zur reinigung bzw. entzunderung von dünnbrammen und bändern in warmbandstrassen, bandbehandlungsanlagen oder dergleichen | |
| DE112013000850T5 (de) | Oberflächenbearbeitungssystem für ein Blechband in kaltem Zustand und Bearbeitungsverfahren für dasselbe | |
| DE102010026757A1 (de) | Verfahren und Produktionslinie zum Herstellen eines kaltgewalzten Stahlflachprodukts aus einem nicht rostenden Stahl | |
| EP2389260B1 (de) | Verfahren und vorrichtung zum glühen und entzundern von band aus nichtrostendem stahl | |
| DE112007002851T5 (de) | Aufbesserungsvorrichtung für Oberflächenrauigkeitsfehler von warm-/kaltgewalzten rostfreien Bandstählen und das diesbezügliche Verfahren | |
| EP3691804A1 (de) | Verfahren zum betrieb einer giess-walz-verbundanlage und giess-walz-verbundanlage | |
| DE4208208C2 (de) | Verfahren und Vorrichtung zur Verminderung der Zunderbildung beim Warmumformen von Metall, insbesondere von Stahl | |
| KR100775297B1 (ko) | 선재코일 제조방법 및 산화막 제거장치 | |
| DE102008039140A1 (de) | Verfahren und Vorrichtung zum Erzeugen eines Magnesiumbands | |
| DE19936010A1 (de) | Verfahren und Vorrichtung zum Unterdrücken von insbesondere Sekundärzunderbildung beim Warmwalzen von Brammen | |
| JP2722105B2 (ja) | ステンレス鋼帯の冷間圧延時の油模様発生防止方法 | |
| JP2689845B2 (ja) | 熱延鋼材の脱スケーリング方法 | |
| KR20020038888A (ko) | 열연강대의 제조방법 및 산화막제거장치 | |
| DE4430856C2 (de) | Verfahren zur Reduzierung und Steuerung der Oberflächenverzunderung beim Warmwalzen von Flachprodukten, insbesondere Warmbändern | |
| EP0523576B1 (de) | Verfahren und Anlage zum Herstellen eines Metallstranges durch Giessen | |
| DE2427329A1 (de) | Verfahren zum beizen von stahl | |
| JPS6061114A (ja) | 快削鋼の圧延方法 | |
| JPH0890051A (ja) | 熱間圧延鋼材のデスケーリング方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20080119 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20080916 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SMS SIEMAG AG |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 502006008740 Country of ref document: DE Date of ref document: 20110224 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502006008740 Country of ref document: DE Effective date: 20110224 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20110112 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2359871 Country of ref document: ES Kind code of ref document: T3 Effective date: 20110527 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20110112 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110512 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110413 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110512 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110412 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 |
|
| 26N | No opposition filed |
Effective date: 20111013 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502006008740 Country of ref document: DE Effective date: 20111013 |
|
| BERE | Be: lapsed |
Owner name: SMS SIEMAG AG Effective date: 20111130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20111117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111117 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20120731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111117 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111118 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 494969 Country of ref document: AT Kind code of ref document: T Effective date: 20111117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111117 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20121121 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111117 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20130715 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111118 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110112 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502006008740 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502006008740 Country of ref document: DE Effective date: 20140603 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140603 |