EP2663497B1 - Verpackungsvorrichtung - Google Patents
Verpackungsvorrichtung Download PDFInfo
- Publication number
- EP2663497B1 EP2663497B1 EP12700061.0A EP12700061A EP2663497B1 EP 2663497 B1 EP2663497 B1 EP 2663497B1 EP 12700061 A EP12700061 A EP 12700061A EP 2663497 B1 EP2663497 B1 EP 2663497B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- packaging
- pack
- products
- loading station
- location
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 238000004806 packaging method and process Methods 0.000 title claims description 97
- 238000010276 construction Methods 0.000 claims description 3
- 230000032258 transport Effects 0.000 description 8
- 238000006243 chemical reaction Methods 0.000 description 5
- 230000008901 benefit Effects 0.000 description 4
- 230000010354 integration Effects 0.000 description 3
- 230000008859 change Effects 0.000 description 2
- 230000006835 compression Effects 0.000 description 2
- 238000007906 compression Methods 0.000 description 2
- 238000012856 packing Methods 0.000 description 2
- 230000006978 adaptation Effects 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 230000008030 elimination Effects 0.000 description 1
- 238000003379 elimination reaction Methods 0.000 description 1
- 238000000265 homogenisation Methods 0.000 description 1
- 238000003780 insertion Methods 0.000 description 1
- 230000037431 insertion Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 238000012546 transfer Methods 0.000 description 1
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B5/00—Packaging individual articles in containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, jars
- B65B5/08—Packaging groups of articles, the articles being individually gripped or guided for transfer to the containers or receptacles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B35/00—Supplying, feeding, arranging or orientating articles to be packaged
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B35/00—Supplying, feeding, arranging or orientating articles to be packaged
- B65B35/30—Arranging and feeding articles in groups
- B65B35/36—Arranging and feeding articles in groups by grippers
- B65B35/38—Arranging and feeding articles in groups by grippers by suction-operated grippers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B35/00—Supplying, feeding, arranging or orientating articles to be packaged
- B65B35/30—Arranging and feeding articles in groups
- B65B35/44—Arranging and feeding articles in groups by endless belts or chains
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B35/00—Supplying, feeding, arranging or orientating articles to be packaged
- B65B35/30—Arranging and feeding articles in groups
- B65B35/50—Stacking one article, or group of articles, upon another before packaging
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/42—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation
- B65B43/48—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation using reciprocating or oscillating pushers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/42—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation
- B65B43/52—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation using roller-ways or endless conveyors
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/42—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation
- B65B43/54—Means for supporting containers or receptacles during the filling operation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B5/00—Packaging individual articles in containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, jars
- B65B5/06—Packaging groups of articles, the groups being treated as single articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B5/00—Packaging individual articles in containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, jars
- B65B5/10—Filling containers or receptacles progressively or in stages by introducing successive articles, or layers of articles
- B65B5/105—Filling containers or receptacles progressively or in stages by introducing successive articles, or layers of articles by grippers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B5/00—Packaging individual articles in containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, jars
- B65B5/10—Filling containers or receptacles progressively or in stages by introducing successive articles, or layers of articles
- B65B5/106—Filling containers or receptacles progressively or in stages by introducing successive articles, or layers of articles by pushers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/001—Arrangements to enable adjustments related to the product to be packaged
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/003—Arrangements to enable adjustments related to the packaging material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/005—Adjustable conveying means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/04—Machines constructed with readily-detachable units or assemblies, e.g. to facilitate maintenance
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
- B65B61/24—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for shaping or reshaping completed packages
Definitions
- the present invention relates to a packaging device for packaging general cargo, in particular in the field of packaging machines.
- Prior art packaging devices generally operate with a transport chain that carries packages or trays through the device. This results in a complex structure and a large footprint. Furthermore, the devices have no modular structure, which allows a simple, rapid and flexible conversion to different packaging sizes and types of packaging, eg. B. with different rankings and layer images of the products in the package allows. Thus, for different applications each specially designed packaging devices must be constructed with considerable time and cost. From the DE 37 20638 A1 is a sophisticated device for filling cartons known to be packaged in trays set tubes.
- US 5,732,536 shows a packaging device according to the preamble of claim 1.
- the packaging device according to the invention with the features of claim 1 has the advantage that it has a plurality of modularly arranged individual modules with few functions, whereby a very robust, simple and inexpensive construction is achieved. Due to the modular structure of the packaging device according to the invention allows the adaptation to a variety of rankings and situation images, z. B. of products with different bag shapes, and also allows a flexible extension to other types of packaging. This is the use especially in the packaging of pillow bags, Doy-style packs and floor packs in all common boxes or trays possible.
- the modular packaging apparatus comprises a packaging feeder for feeding empty packages, a product feeder for feeding products and a loading station, in which the products are packed in the empty package to provide a packaging container. Furthermore, a cardboard outlet is provided, which dissipates the packaging container. Due to the structured structure in individual module areas, a small footprint with small travel paths for loading is also achieved. Thus, smaller and more energy efficient drives can be used.
- the loading station has a first place and a second place, the products being packed in second place in the empty packaging.
- the first and the second place of the loading station are arranged in series on an axis. Furthermore, an axial thrust unit is provided, which acts on the packaging positioned at the first position, in order to push the package located at the second place by means of an axial thrust on the cardboard outlet. Since the packaging push each other further until they reach the cardboard outlet, a transport chain is not required. In addition, the easy and cost-effective loading station enables continuous packaging steps with short cycle times.
- the packaging device preferably comprises a first transverse pushing unit which pushes the empty packaging from the packaging feed to the first place of the loading station.
- the loading station comprises a tilting device, which preferably tilts the packaging by 90 °.
- a horizontal loading of the package without vertical travels is easier and faster feasible.
- a desired horizontal or vertical loading of the packaging may optionally be made.
- the tilting device comprises a support region, wherein one side of the packaging rests on the support region.
- the support area ensures a reliable hold of the packaging during the horizontal loading process in the tilted position. Furthermore, this results in a reliable guidance of the packaging package when pushing in the non-tilted or tilted back position to the cardboard outlet.
- the packaging device comprises a second transverse pushing unit which pushes the products into an empty package at the second place of the loading station.
- the packaging device comprises a vibrating device for shaking the packaging container.
- a compression of the products contained in the package, in particular for bags, is achieved to increase the degree of filling.
- the vibrating device is preferably integrated in the loading station and in this case preferably arranged below the second place of the loading station.
- the packaging feed and the product feed are arranged parallel to one another and the carton outlet is preferably arranged parallel to the packaging feed and product feed.
- the second transverse thrust unit comprises a storage space on which a plurality of products are stored, wherein the second transverse thrust unit common to the intermediately stored products into the packaging in the second place of the loading station.
- Specially required shunting and / or situation images for certain products can thus be produced already at the storage location before insertion into the packaging.
- linear vacuum cleaners, grippers, stacking boxes and slides can be used to display all standard shunting and loading.
- the package feeder comprises a format adjustment, to allow conversion to other packaging formats or carton sizes. This makes a simple, time and cost-efficient conversion or adjustment to other packaging formats possible. In addition, the installation of any necessary format change parts can essentially be done without tools.
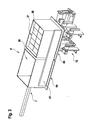
- FIG. 1 shows a schematic perspective view of a packaging device 1 according to the first embodiment of the invention.
- the packaging device 1 comprises a packaging feeder 2, a product feeder 3, a loading station 4 and a cardboard outlet 5.
- a packaging feeder 2a By means of the packaging feeder 2, opened, empty packages 20 are conveyed via a conveyor belt 2a in a first axial direction A1 to a first transverse shear unit arranged axially at the end of the packaging feeder 2 8 transported.
- the packages 20 are guided here on the conveyor belt 2a via left and right guide rails 24a, 24b.
- a format adjustment unit 22 is further provided, which allows by means of spindles 23 an adjustment of the guide rail 24a perpendicular to the first axis direction A1 corresponding to the width of the package 20.
- an adjustment of a stop 25 of the first transverse thrust unit 8 takes place counter to the first axis direction A1. If the Packing 20 has reached the stop 25 in the first transverse shear unit 8, the feed of the packaging feeder 2 is interrupted. A pushing element 8a of the first transverse pushing unit 8 then pushes the package 20 in a fourth axis direction A4 up to a stop element 41 on a first place 4a of the loading station 4 arranged parallel to the first axis direction A1.
- the transport unit 3 arranged parallel to the package feeder 2 transports five products 30, here exemplified in the form of pillow bags, in a third axis direction A3 to a removal position 35.
- a suction device 32 removes the products 30 from the tray 33 and loads in a fifth axis direction A5, the packaging 20 positioned at a second location 4b of the loading station 4 in accordance with a predetermined loading pattern.
- the loading takes place with a fall height "zero", d. H. without dropping the products into the packaging.
- an axial thrust unit 7 advances the empty package 20 in a second axial direction A2 from the first place 4a, which consequently advances the loaded package 20 as packaging package 21 from the second place 4b of the loading station 4 to the carton exit 5 for removal.
- FIG. 2 As can be seen, the first place 4a and the second place 4b of the loading station 4 and the carton outlet 5 are arranged in series on an axis and in the second axis direction A2, respectively.
- the top view of the packaging device 1 serves to illustrate in detail the arrangement relationship of the individual modules with the substantially horizontal transport movements of the packages 20 and the products 30. It should be noted that in FIG. 2 the suction device 32 is not completely shown for clarity.
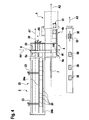
- FIG. 4 shows the packaging device of FIG. 1 with a modified packaging format, wherein the guide rail 24a are adjusted by means of the spindles 23 of the format adjustment unit 22 perpendicular to the first axis direction A1 to the smaller width of the package 20 and by means of the spindle 26 against the first axis direction A1 to the shorter length of the package 20.
- the replacement of the thrust element 8a can be done without tools and the suction unit 32 can be replaced by means of an exchangeable format part.
- the axial thrust unit 7 can be kept identical for all formats and the strokes of the first transverse thrust unit 8 and the axial thrust unit 7 are the same for all formats.
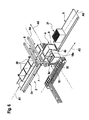
- FIG. 5 a packaging device according to a second preferred embodiment of the invention described in detail.
- the same or functionally identical components are designated here by the same reference numerals as in the first embodiment.
- the packaging apparatus 1 of the second embodiment has a gripping device 34 instead of the suction device 32 used in the first embodiment.
- the gripping device 34 grips the products 30, which are supplied from the product feed 3 in trays 31, to the removal position 35, shown here by way of example in the form of doy-style packs, and positions these in the package 20 in a standing position.
- the packaging device 1 according to the invention can be converted simply by adapting the module of the product feeder 3 together with the inserted trays 31 and the gripping device 34 in a simple manner to the changed product shape and its position and ranking in the packaging 20.
- the other modules of the packaging device 1 can be kept unchanged.
- the unchanged small base area for the line integration is of particular advantage here.
- FIGS. 6 to 8 a packaging device according to a third preferred embodiment of the invention in detail described.
- the same or functionally identical components are designated here by the same reference numerals as in the first embodiment.
- the packaging apparatus according to the third embodiment has substantially the same arrangement as that of the first embodiment.
- the packaging device 1 of the third exemplary embodiment comprises a second transverse pushing unit 10 with a storage space 10a into which the products 30 (pillow-type or doy-style packs) are introduced or stored in a stack by means of the suction device 32.
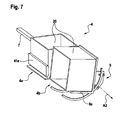
- a tilting device 9 is provided, which is provided at the second place 4b of the loading station 4. How detailed FIG. 7 and FIG.
- the empty package 20 positioned in the second position 4b of the loading station 4 can be tilted by 90 ° counterclockwise by means of the tilting device 9 with respect to the second axis direction A2, so that the opening of the package 20 is positioned substantially horizontally.
- the second transverse pushing unit 10 pushes horizontally into the package 20 the (stacked) products 30 temporarily stored at the storage space 10a.
- the tilting device 9 for further transport of the packaging back into the in FIG. 8 shown not tilted position brought.
- the tilting device 9 furthermore has a support region 9a arranged perpendicular to the bottom surface of the packaging 20, against which one side of the packaging 20 rests and is supported during the tilting movement.
- the support region 9a in the region of the second space 4b together with a shortened stop element 41a in the region of the first place 4a of the loading station 4 serves as a guide for the displacement of the packages 20 by means of the axial thrust unit 7.
- packaging container 21 can be made with vertically loaded pillow bags or Doy-style packs.
- the remaining modules used in the first embodiment can be kept unchanged.
- the transfer or travel paths of the suction device 32 are substantially simpler and shorter than those of the gripping device 34 in the second embodiment. The conversion to the changed situation and ranking of the products can with very short Standstill or changeover times of the system and minimal personnel and costs are performed.
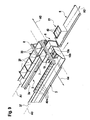
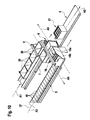
- FIG. 9 a packaging device according to a fourth preferred embodiment of the invention described in detail. Identical or functionally identical components are designated here by the same reference numerals as in the preceding embodiments.
- products 40 in the form of floor packings, which are supplied in the form of floor packs, are supplied from the product feeder 3 to the second transverse pushing device 10 arranged at the end of the product feeder 3 in the third axis direction A3.
- a guide rail 37 arranged in the transport direction or the third axis direction A3 aligns the products 40 in an axially aligned manner with respect to one another.
- the second transverse thrust device 10 has an end stop 10b and pushes three products 40 in the fifth axis A5 in the same as in the third embodiment tilted packaging 20.
- the fully loaded package 20 is then rotated back to the non-tilted position and as packaging container 21 with horizontal Loading transported via the cardboard outlet 5.
- no suction device or gripping device is required, so that shorter cycle times for the loading of the packaging 20 can be realized.
- FIG. 10 a packaging device according to a fifth preferred embodiment of the invention described in detail.
- Identical or functionally identical components are here designated by the same reference numerals as in the preceding embodiments, wherein the products are also floor packs.
- the packaging apparatus 1 of the fifth embodiment has here, with the exception of the width of the guide rail 37, substantially the same arrangement and advantages as that of the fourth Embodiment on. Starting from the fourth embodiment, therefore, a conversion of the situation image of the packaged products 40 without significant effort at short notice feasible.
- the packaging devices 1 according to the invention described in the exemplary embodiments have the advantage that due to the modular design with a few simple functions essentially all current bags or product packaging can be packed with all horizontal and vertical routing and different layer images in all popular cartons. Furthermore, a flexible format change as well as a simplified extension to future types of packaging and applications is possible. The elimination of transport chains also short travel paths and a small footprint required for line integration can be realized.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Microelectronics & Electronic Packaging (AREA)
- Container Filling Or Packaging Operations (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
Description
- Die vorliegende Erfindung betrifft eine Verpackungsvorrichtung zum Verpacken von Stückgut insbesondere im Bereich von Verpackungsmaschinen.
- Verpackungsvorrichtungen des Standes der Technik arbeiten im Allgemeinen mit einer Transportkette, die Verpackungen oder Trays durch die Vorrichtung transportieren. Hieraus resultieren ein aufwendiger Aufbau sowie ein großer Platzbedarf. Ferner besitzen die Vorrichtungen keinen modularen Aufbau, der eine einfache, rasche und flexible Umrüstung auf verschiedene Verpackungsgrößen und Verpackungsarten, z. B. mit unterschiedlichen Rangierungen und Lagenbildern der Produkte in der Verpackung, ermöglicht. Somit müssen für unterschiedliche Anwendungen jeweils speziell konstruierte Verpackungsvorrichtungen mit erheblichem Zeit- und Kostenaufwand aufgebaut werden. Aus der
DE 37 20638 A1 ist eine aufwändige Vorrichtung zum Befüllen von Kartons bekannt, bei der in Trays eingestellte Tuben verpackt werden. -
US 5,732,536 zeigt eine Verpackungsvorrichtung gemäß dem Oberbegriff des Anspruchs 1. - Die erfindungsgemäße Verpackungsvorrichtung mit den Merkmalen des Anspruchs 1 weist demgegenüber den Vorteil auf, dass diese mehrere modular angeordnete Einzelbaugruppen mit wenigen Funktionen aufweist, wodurch ein sehr robuster, einfacher und kostengünstiger Aufbau erreicht wird. Durch den modularen Aufbau ermöglicht die erfindungsgemäße Verpackungsvorrichtung die Anpassung an eine Vielzahl von Rangierungen und Lagebildern, z. B. von Produkten mit unterschiedlichen Beutelformen, und ermöglicht ferner eine flexible Erweiterung auf andere Verpackungsarten. Hierdurch ist der Einsatz insbesondere bei der Verpackung von Kissenbeuteln, Doy-Style-Packungen und Standbodenpackungen in allen gängigen Kartons oder Trays möglich. Dies wird erfindungsgemäß dadurch erreicht, dass die modular aufgebaute Verpackungsvorrichtung eine Verpackungszuführung zum Zuführen von leeren Verpackungen, eine Produktzuführung zum Zuführen von Produkten und eine Beladestation aufweist, in welcher die Produkte in die leere Verpackung gepackt werden, um ein Verpackungsgebinde bereitzustellen. Ferner ist ein Kartonauslauf vorgesehen, welcher das Verpackungsgebinde abführt. Durch den strukturierten Aufbau in einzelne Modulbereiche wird ferner eine kleine Grundfläche mit kleinen Verfahrwegen zur Beladung erreicht. Somit können kleinere und energieeffizientere Antriebe zum Einsatz kommen.
- Gemäß der Erfindung weist die Beladestation einen ersten Platz und einem zweiten Platz auf, wobei die Produkte am zweiten Platz in die leere Verpackung gepackt werden.
- Erfindungsgemäß sind der erste und der zweite Platz der Beladestation in Reihe auf einer Achse angeordnet. Ferner ist eine Axialschubeinheit vorgesehen, welche an der am ersten Platz positionierten Verpackung angreift, um das am zweiten Platz befindliche Verpackungsgebinde mittels eines Axialschubs auf den Kartonauslauf zu schieben. Da sich die Verpackungen gegenseitig weiterschieben, bis sie den Kartonauslauf erreichen, ist eine Transportkette nicht erforderlich. Zudem ermöglicht die einfach und kostengünstig aufgebaute Beladestation kontinuierliche Verpackungsschritte mit kurzen Taktzeiten.
- Die Unteransprüche zeigen bevorzugte Weiterbildungen der Erfindung.
- Bevorzugt umfasst die Verpackungsvorrichtung eine erste Querschubeinheit, welche die leere Verpackung von der Verpackungszuführung auf den ersten Platz der Beladestation schiebt. Hierdurch wird eine einfache und betriebssichere Beschickung der Beladestation erreicht. Das geringe Eigengewicht der Verpackung sowie der niedrige Reibungswiderstand beim horizontalen Verschieben ermöglichen zudem den Einsatz von kleinen, kostengünstigen Antriebsmotoren für die erste Querschubeinheit.
- In weiterer vorteilhafter Ausgestaltung der Erfindung umfasst die Beladestation eine Kippeinrichtung, welche die Verpackung vorzugsweise um 90° kippt. Hierdurch ist eine horizontale Beladung der Verpackung ohne vertikale Verfahrwege einfacher und schneller durchführbar. Ferner kann ohne eine Umrüstung der Verpackungsvorrichtung wahlweise eine gewünschte horizontale oder vertikale Beladung der Verpackung erfolgen.
- Weiterhin bevorzugt umfasst die Kippeinrichtung einen Abstützbereich, wobei eine Seite der Verpackung am Abstützbereich anliegt. Der Abstützbereich gewährleistet einen betriebssicheren Halt der Verpackung beim horizontalen Beladungsvorgang in der gekippten Stellung. Ferner wird hierdurch eine zuverlässige Führung des Verpackungsgebindes beim Schieben in der nicht bzw. zurück gekippten Stellung zum Kartonauslauf erreicht.
- Weiterhin bevorzugt umfasst die Verpackungsvorrichtung eine zweite Querschubeinheit, welche die Produkte in eine leere Verpackung am zweiten Platz der Beladestation schiebt. Hierdurch kann mit minimiertem Bauaufwand und sehr kurzer Schubdistanz eine horizontale Beladung der Verpackung realisiert werden.
- In weiterer vorteilhafter Ausgestaltung der Erfindung umfasst die Verpackungsvorrichtung eine Rütteleinrichtung zum Rütteln des Verpackungsgebindes. Hierdurch wird eine Verdichtung der in der Verpackung befindlichen Produkte, insbesondere bei Beuteln, zur Erhöhung des Füllgrads erreicht. Die Rütteleinrichtung ist vorzugsweise in die Beladestation integriert und hierbei vorzugsweise unter dem zweiten Platz der Beladestation angeordnet.
- Weiterhin bevorzugt sind die Verpackungszuführung und die Produktzuführung parallel zueinander angeordnet und der Kartonauslauf vorzugsweise parallel zur Verpackungszuführung und Produktzuführung angeordnet. Hierdurch wird eine optimierte Linieneinbindung mit einer minimierten Grundfläche der gesamten Verpackungsvorrichtung erreicht.
- Weiterhin bevorzugt umfasst die zweite Querschubeinheit einen Bevorratungsplatz, an welchem mehrere Produkte zwischengelagert werden, wobei die zweite Querschubeinheit die zwischengelagerten Produkte gemeinsam in die Verpackung am zweiten Platz der Beladestation schiebt. Speziell erforderliche Rangierungen und/oder Lagebilder bei bestimmten Produkten können somit bereits am Bevorratungsplatz vor dem Einschub in die Verpackung hergestellt werden. Je nach Lagenbild können hierfür Linearsauger, Greifer, Stapelkasten und Schieber eingesetzt werden, über die alle gängigen Rangierungen und Beladungen darstellbar sind.
- In weiterer vorteilhafter Ausgestaltung der Erfindung umfasst die Verpackungszuführung eine Formatverstelleinheit, um eine Umstellung auf andere Verpackungsformate bzw. Kartongrößen zu ermöglichen. Hiermit ist eine einfache, zeit- und kosteneffiziente Umstellung bzw. Justierung auf andere Verpackungsformate möglich. Zudem kann der Einbau von ggf. erforderlichen Formatwechselteilen im Wesentlichen werkzeuglos erfolgen.
- Nachfolgend werden Ausführungsbeispiele der Erfindung unter Bezugnahme auf die begleitende Zeichnung im Detail beschrieben. In der Zeichnung ist:
- Figur 1
- eine schematische Perspektivansicht einer Verpackungsvorrichtung gemäß einem ersten Ausführungsbeispiel der Erfindung,
- Figur 2
- eine schematische Draufsicht der Vorrichtung von
Figur 1 - Figur 3
- eine perspektivische Ansicht einer Beladestation der Vorrichtung von
Figur 1 , - Figur 4
- eine Draufsicht auf die Verpackungsvorrichtung von
Figur 1 mit verändertem Verpackungsformat, - Figur 5
- eine perspektivische Teilansicht der Verpackungsvorrichtung gemäß einem zweiten Ausführungsbeispiel der Erfindung,
- Figur 6
- eine schematische Perspektivansicht der Verpackungsvorrichtung gemäß einem dritten Ausführungsbeispiel der Erfindung,
- Figur 7
- eine perspektivische Ansicht einer Kippeinrichtung der Verpackungsvorrichtung von
Figur 5 in gekippter Stellung, - Figur 8
- eine perspektivische Ansicht der Kippeinrichtung von
Figur 6 in nicht gekippter Stellung, - Figur 9
- eine perspektivische Teilansicht der Verpackungsvorrichtung gemäß einem vierten Ausführungsbeispiel der Erfindung, und
- Figur 10
- perspektivische Teilansicht der Verpackungsvorrichtung gemäß einem fünften Ausführungsbeispiel der Erfindung.
- Nachfolgend wird unter Bezugnahme auf
Figur 1 bis 4 eine modular aufgebaute Verpackungsvorrichtung gemäß einem ersten bevorzugten Ausführungsbeispiel der Erfindung im Detail beschrieben. -
Figur 1 zeigt eine schematische Perspektivansicht einer Verpackungsvorrichtung 1 gemäß dem ersten Ausführungsbeispiel der Erfindung. Die Verpackungsvorrichtung 1 umfasst eine Verpackungszuführung 2, eine Produktzuführung 3, eine Beladestation 4 und einen Kartonauslauf 5. Mittels der Verpackungszuführung 2 werden geöffnete, leere Verpackungen 20 über ein Transportband 2a in einer ersten Achsenrichtung A1 zu einer axial am Ende der Verpackungszuführung 2 angeordneten ersten Querschubeinheit 8 transportiert. Die Verpackungen 20 werden hierbei auf dem Transportband 2a über linke und rechte Führungsschienen 24a, 24b geführt. An der Verpackungszuführung 2 ist ferner eine Formatverstelleinheit 22 vorgesehen, die mittels Spindeln 23 eine Verstellung der Führungsschiene 24a senkrecht zur ersten Achsenrichtung A1 entsprechend der Breite der Verpackung 20 ermöglicht. Mittels einer weiteren Spindel 26 erfolgt eine Verstellung eines Anschlags 25 der ersten Querschubeinheit 8 entgegen der ersten Achsenrichtung A1. Wenn die Verpackung 20 den Anschlag 25 in der ersten Querschubeinheit 8 erreicht hat, wird der Vorschub der Verpackungszuführung 2 unterbrochen. Ein Schubelement 8a der ersten Querschubeinheit 8 schiebt danach die Verpackung 20 in einer vierten Achsenrichtung A4 bis zu einem Anschlagelement 41 auf einen ersten Platz 4a der parallel zur ersten Achsenrichtung A1 angeordneten Beladestation 4. - Die parallel zur Verpackungszuführung 2 angeordnete Transporteinheit 3 transportiert jeweils fünf in einem Tray 33 aufgenommene Produkte 30, hier beispielhaft in Form von Kissenbeuteln dargestellt, in einer dritten Achsenrichtung A3 zu einer Entnahmeposition 35. Eine Saugeinrichtung 32 entnimmt die Produkte 30 aus dem Tray 33 und belädt damit in einer fünften Achsenrichtung A5 die auf einem zweiten Platz 4b der Beladungstation 4 positionierte Verpackung 20 entsprechend einem vorgegebenen Belademuster. Hierbei erfolgt die Beladung mit einer Fallhöhe "Null", d. h. ohne Abwerfen der Produkte in die Verpackung.
- Nach dem Beladen schiebt eine Axialschubeinheit 7 die leere Verpackung 20 in einer zweiten Achsenrichtung A2 vom ersten Platz 4a weiter, die demzufolge die beladene Verpackung 20 als Verpackungsgebinde 21 vom zweiten Platz 4b der Beladestation 4 auf den Kartonauslauf 5 zum Abtransport weiterschiebt. Wie aus
Figur 2 ersichtlich, sind der erste Platz 4a und der zweite Platz 4b der Beladestation 4 und der Kartonsauslauf 5 in Reihe auf einer Achse bzw. in der zweiten Achsenrichtung A2 angeordnet. Die inFigur 2 dargestellte Draufsicht der Verpackungsvorrichtung 1 dient der detaillierten Veranschaulichung der Anordnungsbeziehung der einzelnen Module mit den im Wesentlichen horizontalen Transportbewegungen der Verpackungen 20 und der Produkte 30. Hierbei sei angemerkt, dass inFigur 2 die Saugeinrichtung 32 zur besseren Übersichtlichkeit nicht vollständig dargestellt ist. - Wie aus
Figur 3 ersichtlich, ist unter dem zweiten Platz 4b der Beladestation 4 eine Rütteleinrichtung 12 zum Rütteln der Verpackung 20 während dem Beladen vorgesehen. Hierdurch erfolgen eine Verdichtung der Produkte 30 in der Verpackung 20 sowie eine Homogenisierung der Lagen, die den Füllgrad erhöht.Figur 4 zeigt die Verpackungsvorrichtung vonFigur 1 mit verändertem Verpackungsformat, wobei die Führungsschiene 24a mittels der Spindeln 23 der Formatverstelleinheit 22 senkrecht zur ersten Achsenrichtung A1 auf die geringere Breite der Verpackung 20 und mittels der Spindel 26 entgegen der ersten Achsenrichtung A1 auf die geringere Länge der Verpackung 20 verstellt sind. Bei der Formatumstellung kann der Austausch des Schubelements 8a werkzeuglos erfolgen und die Saugeinheit 32 mittels eines austauschbaren Formatteils ersetzt werden. Hierbei sei angemerkt, dass die Axialschubeinheit 7 für alle Formate identisch beibehalten werden kann und die Hübe der ersten Querschubeinheit 8 sowie der Axialschubeinheit 7 für alle Formate gleich sind. - Nachfolgend wird mit Bezug auf
Figur 5 eine Verpackungsvorrichtung gemäß einem zweiten bevorzugten Ausführungsbeispiel der Erfindung detailliert beschrieben. Gleiche oder funktional gleiche Bauteile sind hier mit denselben Bezugszeichen wie im ersten Ausführungsbeispiel bezeichnet. - Im Gegensatz zum zuvor beschriebenen ersten Ausführungsbeispiel weist die Verpackungsvorrichtung 1 des zweiten Ausführungsbeispiels eine Greifeinrichtung 34 anstelle der der im ersten Ausführungsbeispiel verwendeten Saugeinrichtung 32 auf. Die Greifeinrichtung 34 greift die von der Produktzuführung 3 in Trays 31 stehend der Entnahmeposition 35 zugeführten Produkte 30, hier beispielhaft in Form von Doy-Style-Packungen dargestellt, und positioniert diese stehend in die Verpackung 20.
- Wie aus
Figur 5 ersichtlich, kann die erfindungsgemäße Verpackungsvorrichtung 1 lediglich durch eine Anpassung des Moduls der Produktzuführung 3 samt den eingesetzten Trays 31 sowie der Greifeinrichtung 34 auf einfache Weise auf die veränderte Produktform und deren Lage und Rangierung in der Verpackung 20 umgestellt werden. Die anderen Module der Verpackungsvorrichtung 1 können unverändert beibehalten werden. Neben den sehr kurzen Rüstzeiten ist hierbei auch die unverändert kleine Grundfläche für die Linieneinbindung von besonderem Vorteil. - Nachfolgend wird mit Bezug auf die
Figuren 6 bis 8 eine Verpackungsvorrichtung gemäß einem dritten bevorzugten Ausführungsbeispiel der Erfindung detailliert beschrieben. Gleiche oder funktional gleiche Bauteile sind hier mit denselben Bezugszeichen wie im ersten Ausführungsbeispiel bezeichnet. - Die Verpackungsvorrichtung gemäß dem dritten Ausführungsbeispiel weist im Wesentlichen die gleiche Anordnung wie die des ersten Ausführungsbeispiels auf. Im Unterschied zum ersten Ausführungsbeispiel umfasst die Verpackungsvorrichtung 1 des dritten Ausführungsbeispiels jedoch eine zweite Querschubeinheit 10 mit einem Bevorratungsplatz 10a, in den die Produkte 30 (Kissenbeutel bzw. Doy-Style-Packungen) mittels der Saugeinrichtung 32 gestapelt eingebracht bzw. zwischengelagert werden. Ferner ist eine Kippeinrichtung 9 vorgesehen, die am zweiten Platz 4b der Beladungsstation 4 vorgesehen ist. Wie detailliert aus
Figur 7 undFigur 8 ersichtlich, kann die auf dem zweiten Platz 4b der Beladungsstation 4 positionierte leere Verpackung 20 mittels der Kippeinrichtung 9 in Bezug auf die zweite Achsenrichtung A2 entgegen dem Uhrzeigersinn um 90° gekippt werden, sodass die Öffnung der Verpackung 20 im Wesentlichen horizontal positioniert ist. In dieser gekippten Stellung schiebt die zweite Querschubeinheit 10 die am Bevorratungsplatz 10a zwischengelagerten (gestapelten) Produkte 30 horizontal in die Verpackung 20 ein. Danach wird die Kippeinrichtung 9 zum Weitertransport der Verpackung wieder in die inFigur 8 dargestellte nicht gekippte Stellung gebracht. Die Kippeinrichtung 9 weist ferner einen senkrecht zur Bodenfläche der Verpackung 20 angeordneten Abstützbereich 9a auf, an welchem eine Seite der Verpackung 20 anliegt und bei der Kippbewegung abgestützt wird. In der nicht gekippten Stellung dient der Abstützbereich 9a im Bereich des zweiten Platzes 4b zusammen mit einem hier verkürzt ausgeführten Anschlagelement 41 a im Bereich des ersten Platzes 4a der Beladungsstation 4 als Führung für die Verschiebung der Verpackungen 20 mittels der Axialschubeinheit 7. - Mittels der durch die zweite Querschubeinheit 10 und die Kippeinrichtung 9 erweiterten Beladungsstation 4 können somit Verpackungsgebinde 21 mit vertikal beladenen Kissenbeuteln bzw. Doy-Style-Packungen hergestellt werden. Hierbei können die die im ersten Ausführungsbeispiel verwendeten restlichen Module unverändert beibehalten werden. Ferner sind die Transfer- bzw. Verfahrwege der Saugeinrichtung 32 hierbei wesentlich einfacher und kürzer als die der Greifeinrichtung 34 im zweiten Ausführungsbeispiel. Die Umstellung auf die geänderte Lage und Rangierung der Produkte kann mit sehr kurzen Stillstand- bzw. Umrüstzeiten der Anlage und minimalem Personal- und Kostenaufwand durchgeführt werden.
- Nachfolgend wird mit Bezug auf
Figur 9 eine Verpackungsvorrichtung gemäß einem vierten bevorzugten Ausführungsbeispiel der Erfindung detailliert beschrieben. Gleiche oder funktional gleiche Bauteile sind hier mit denselben Bezugszeichen wie in den vorhergehenden Ausführungsbeispielen bezeichnet. - Bei diesem vierten Ausführungsbeispiel werden von der Produktzuführung 3 stehend zugeführte Produkte 40, in Form von Standbodenpackungen, der hierbei in der dritten Achsenrichtung A3 am Ende der Produktzuführung 3 angeordneten zweiten Querschubeinrichtung 10 zugeführt. Eine in Transportrichtung bzw. der dritten Achsenrichtung A3 angeordnete Führungsschiene 37 richtet die Produkte 40 zueinander axial fluchtend aus. Die zweite Querschubeinrichtung 10 weist einen Endanschlag 10b auf und schiebt jeweils drei Produkte 40 in der fünften Achsenrichtung A5 in die gleichermaßen wie im dritten Ausführungsbeispiel gekippte Verpackung 20. Die vollständig beladene Verpackung 20 wird dann in die nicht gekippte Stellung zurückgedreht und als Verpackungsgebinde 21 mit horizontaler Beladung über den Kartonauslauf 5 abtransportiert. Im Gegensatz zu den zuvor beschriebenen Ausführungsbeispielen ist hierbei keine Saugeinrichtung oder Greifeinrichtung erforderlich, sodass kürzere Taktzeiten für die Beladung der Verpackung 20 realisiert werden können.
- Nachfolgend wird mit Bezug auf
Figur 10 eine Verpackungsvorrichtung gemäß einem fünften bevorzugten Ausführungsbeispiel der Erfindung detailliert beschrieben. Gleiche oder funktional gleiche Bauteile sind hier mit denselben Bezugszeichen wie in den vorhergehenden Ausführungsbeispielen bezeichnet, wobei die Produkte ebenfalls Standbodenpackungen sind. - Im Gegensatz zum zuvor beschriebenen vierten Ausführungsbeispiel werden hierbei die von der Produktzuführung 3 liegend zugeführten Produkte 40 liegend in die gekippte Verpackung 20 gepackt, das Verpackungsgebinde 21 zurückgekippt und als Verpackungsgebinde 21 mit vertikaler Beladung abtransportiert. Die Verpackungsvorrichtung 1 des fünften Ausführungsbeispiels weist hierbei, mit Ausnahme der Breite der Führungsschiene 37, im Wesentlichen die gleiche Anordnung sowie Vorteile wie die des vierten Ausführungsbeispiels auf. Ausgehend vom vierten Ausführungsbeispiel ist daher eine Umstellung des Lagebilds der verpackten Produkte 40 ohne nennenswerten Aufwand kurzfristig durchführbar.
- Die in den Ausführungsbeispielen beschriebenen erfindungsgemäßen Verpackungsvorrichtungen 1 weisen den Vorteil auf, dass aufgrund des modularen Aufbaus mit wenigen einfachen Funktionen im Wesentlichen alle gängigen Beutel bzw. Produktverpackungen mit jeweils horizontaler als auch vertikaler Rangierung sowie verschiedenen Lagenbildern in alle gängigen Kartons verpackt werden können. Ferner ist eine flexible Formatumstellung sowie eine vereinfachte Erweiterung auf zukünftige Packungsarten und Anwendungen möglich. Durch den Entfall von Transportketten sind zudem kurze Verfahrwege sowie eine geringe erforderliche Grundfläche zur Linieneinbindung realisierbar.
Claims (9)
- Modular aufgebaute Verpackungsvorrichtung, umfassend die folgenden Module :- eine Verpackungszuführung (2) zum Zuführen von leeren Verpackungen (20),- eine Produktzuführung (3) zum Zuführen von Produkten (30, 40),- eine Beladestation (4), in welcher die Produkte (30, 40) in die leere Verpackung (20) gepackt werden, um ein Verpackungsgebinde (21) bereitzustellen, und- einen Kartonauslauf (5), welcher das Verpackungsgebinde (21) abführt,dadurch gekennzeichnet, dass- die Beladestation (4) einen ersten Platz (4a) und einen zweiten Platz (4b) aufweist, wobei die Produkte (30, 40) am zweiten Platz (4b) in die leere Verpackung (20) gepackt werden, und wobei- der erste und zweite Platz (4a, 4b) der Beladestation (4) in Reihe auf einer Achse (A2) angeordnet sind und eine Axialschubeinheit (7) vorgesehen ist, welche an der am ersten Platz positionierten Verpackung (20) angreift, um das am zweiten Platz (4b) befindliche Verpackungsgebinde (21) mittels eines Axialschubs auf den Kartonauslauf (5) zu schieben.
- Verpackungsvorrichtung nach Anspruch 1, ferner umfassend eine erste Querschubeinheit (8), welche die leere Verpackung (20) von der Verpackungszuführung (2) auf den ersten Platz (4a) der Beladestation (4) schiebt.
- Verpackungsvorrichtung nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Beladestation (4) eine Kippeinrichtung (9) umfasst, und die leere Verpackung (20) vorzugsweise um 90° kippt.
- Verpackungsvorrichtung nach Anspruch 3, dadurch gekennzeichnet, dass die Kippeinrichtung (9) einen Abstützbereich (9a) umfasst, wobei eine Seite der Verpackung (20) am Abstützbereich (9a) anliegt.
- Verpackungsvorrichtung nach einem der vorhergehenden Ansprüche, ferner umfassend eine zweite Querschubeinheit (10), welche die Produkte (30, 40) in eine leere Verpackung (20) am zweiten Platz (4b) der Beladestation (4) schiebt.
- Verpackungsvorrichtung nach einem der vorhergehenden Ansprüche, ferner umfassend eine Rütteleinrichtung (12) zum Rütteln des Verpackungsgebindes (21).
- Verpackungsvorrichtung nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Verpackungszuführung (2) und die Produktzuführung (3) zueinander parallel angeordnet sind und der Kartonauslauf (5) vorzugsweise parallel zur Verpackungszuführung (2) und Produktzuführung (3) angeordnet ist.
- Verpackungsvorrichtung nach einem der Ansprüche 5 bis 7, dadurch gekennzeichnet, dass die zweite Querschubeinheit (10) einen Bevorratungsplatz (10a) umfasst, an welchem mehrere Produkte (30, 40) zwischengelagert werden, wobei die zweite Querschubeinheit (10) die zwischengelagerten Produkte (30, 40) gemeinsam in die Verpackung (20) am zweiten Platz (4b) der Beladestation (4) schiebt.
- Verpackungsvorrichtung nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Verpackungszuführung (2) eine Formatverstelleinheit (22) umfasst, um eine Umstellung auf andere Verpackungsformate zu ermöglichen.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102011002575A DE102011002575A1 (de) | 2011-01-12 | 2011-01-12 | Verpackungsvorrichtung |
| PCT/EP2012/050030 WO2012095332A1 (de) | 2011-01-12 | 2012-01-03 | Verpackungsvorrichtung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2663497A1 EP2663497A1 (de) | 2013-11-20 |
| EP2663497B1 true EP2663497B1 (de) | 2014-11-05 |
Family
ID=45463615
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12700061.0A Not-in-force EP2663497B1 (de) | 2011-01-12 | 2012-01-03 | Verpackungsvorrichtung |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20130283731A1 (de) |
| EP (1) | EP2663497B1 (de) |
| CN (1) | CN103298696B (de) |
| BR (1) | BR112013017599A2 (de) |
| DE (1) | DE102011002575A1 (de) |
| WO (1) | WO2012095332A1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US10414528B2 (en) | 2015-05-29 | 2019-09-17 | Graphic Packaging International, Llc | Packaging system |
Families Citing this family (50)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US8813950B2 (en) * | 2010-05-07 | 2014-08-26 | The Procter & Gamble Company | Automated adjustment system for star wheel |
| ES2684369T3 (es) * | 2011-11-15 | 2018-10-02 | Adaptapack Pty Limited | Un conjunto de empaquetado |
| CN103057752B (zh) * | 2012-12-28 | 2015-04-29 | 长沙众能自控科技有限公司 | 长条状舟皿供给装置及供给方法 |
| DE102013105002A1 (de) * | 2013-05-15 | 2014-11-20 | Focke & Co. (Gmbh & Co. Kg) | Verfahren zur Handhabung von Behältern, insbesondere Kartons, für Gruppen von Gegenständen, insbesondere Packungen |
| DE102013009229B4 (de) | 2013-05-31 | 2017-02-23 | Meurer Verpackungssysteme Gmbh | Verpackungsmaschine |
| DE102013212329A1 (de) * | 2013-06-26 | 2014-12-31 | Robert Bosch Gmbh | Verpackung von biegeschlaffen Bauteilen |
| CN105015841A (zh) * | 2014-04-23 | 2015-11-04 | 磊登自动控制有限公司 | 盒装产品包装机 |
| JP6465561B2 (ja) * | 2014-04-24 | 2019-02-06 | 株式会社アイディエス | 容器回収装置及び容器回収装置を用いた尿検査装置 |
| US11059185B2 (en) * | 2014-10-03 | 2021-07-13 | Frito-Lay North America, Inc. | Apparatus and method for transferring a pattern from a universal surface to an ultimate package |
| DE102014221218A1 (de) * | 2014-10-20 | 2016-04-21 | Krones Aktiengesellschaft | Vorrichtung und Verfahren zum Umgang mit Artikeln |
| DE102014221232A1 (de) * | 2014-10-20 | 2016-04-21 | Krones Aktiengesellschaft | Vorrichtung und Verfahren zum Umgang mit Artikeln |
| DE102014221233A1 (de) | 2014-10-20 | 2016-04-21 | Krones Aktiengesellschaft | Vorrichtung und Verfahren zum Umgang mit Artikeln |
| JP6463147B2 (ja) * | 2015-01-23 | 2019-01-30 | 株式会社イシダ | 箱詰め装置 |
| CN106275541B (zh) * | 2015-05-21 | 2019-02-01 | 广州市博仕机电工贸有限公司 | 一种圆柱条状物料层叠装箱机 |
| TWI549890B (zh) * | 2015-08-27 | 2016-09-21 | 全利機械股份有限公司 | 成列產品之堆疊裝置 |
| US10759550B2 (en) * | 2015-09-25 | 2020-09-01 | Douglas Machine Inc. | Intermittent case packer assembly and methods |
| KR102664260B1 (ko) * | 2015-12-07 | 2024-05-08 | 프리메탈스 테크놀로지스 유에스에이 엘엘씨 | 코일 진동 시스템 |
| US10981683B2 (en) * | 2015-12-25 | 2021-04-20 | Ishida Co., Ltd. | Boxing apparatus |
| ITUA20163016A1 (it) * | 2016-04-29 | 2017-10-29 | Ilapak Int Sa | Macchina per il confezionamento sottovuoto. |
| JP6792856B2 (ja) * | 2016-07-12 | 2020-12-02 | 株式会社イシダ | 箱詰め装置 |
| DE102016014333A1 (de) * | 2016-12-02 | 2018-06-07 | Focke & Co. (Gmbh & Co. Kg) | Verfahren und Vorrichtung zum Befüllen eines Behälters mit Produkten |
| IT201600130241A1 (it) * | 2016-12-22 | 2018-06-22 | Gefin Srl | Macchina per l'imballaggio di gabbiette porta tappo |
| CN106697406A (zh) * | 2016-12-27 | 2017-05-24 | 天津电气科学研究院有限公司 | 一种多工位转盘灌装设备 |
| IT201700059046A1 (it) * | 2017-05-30 | 2018-11-30 | Mad Automation Srl | Macchina incartonatrice. |
| CN107284737A (zh) * | 2017-06-09 | 2017-10-24 | 安徽中能电源有限公司 | 蓄电池半自动电池装箱机及装箱方法 |
| DE102017114760A1 (de) * | 2017-07-03 | 2019-01-03 | Sig Technology Ag | Zellentraverse mit Einsatzelementen für eine Füllmaschine |
| DE202017104350U1 (de) | 2017-07-20 | 2018-08-22 | Rudholzer Technologien GmbH | Packeinrichtung mit verstellbarer Größe |
| CN109835548B (zh) * | 2017-11-27 | 2024-08-27 | 湖南楚天华兴智能装备有限公司 | 物料自动输送装置 |
| JP7180857B2 (ja) * | 2018-02-27 | 2022-11-30 | 株式会社イシダ | 製函・箱詰め・封函装置 |
| CN108910106A (zh) * | 2018-06-28 | 2018-11-30 | 南京华腾汽配有限公司 | 一种汽车零部件包装装置 |
| CN109250169A (zh) * | 2018-08-24 | 2019-01-22 | 安徽麦德发食品有限公司 | 一种方便面装箱机 |
| CN109533462A (zh) * | 2018-11-16 | 2019-03-29 | 贵州雅光电子科技股份有限公司 | 一种二极管引线自动夹料装置及方法 |
| CN109367860B (zh) * | 2018-12-05 | 2021-07-13 | 安徽侬安康食品有限公司 | 一种烘烤饼干冷却分拣包装一体装置 |
| CN109625442A (zh) * | 2018-12-05 | 2019-04-16 | 安徽侬安康食品有限公司 | 一种烘烤饼干分拣用包装盒推送装置 |
| CN113613999B (zh) * | 2019-01-10 | 2023-08-04 | Abb瑞士股份公司 | 包装单元和方法 |
| CN113022913B (zh) * | 2019-12-09 | 2023-03-31 | 中国兵器装备集团自动化研究所 | 一种用于枪弹自动包装线的非连续纸盒的布弹装置和方法 |
| CN111977072A (zh) * | 2020-09-07 | 2020-11-24 | 李维全 | 一种肥皂快速自动包装装置 |
| NL2026455B1 (en) * | 2020-09-11 | 2022-05-12 | Moba Group Bv | A system and method for handling packaging units, and manipulator unit. |
| CN113022957B (zh) * | 2021-02-09 | 2023-05-09 | 廊坊京磁精密材料有限公司 | 侧立码料装盒机构和侧立码料装盒机 |
| US20220306326A1 (en) * | 2021-03-26 | 2022-09-29 | Proseal Uk Limited | Tray positioning and loading system |
| DE102021107944A1 (de) * | 2021-03-30 | 2022-10-06 | Multivac Sepp Haggenmüller Se & Co. Kg | Verfahren zum Einlegen von Produkten in Trays und Beladestation |
| CN113086310A (zh) * | 2021-04-10 | 2021-07-09 | 安徽省无为县曙光羽毛制品有限公司 | 一种制备羽毛球后的入料包装装置 |
| JP2023028584A (ja) * | 2021-08-19 | 2023-03-03 | サンワテクノス株式会社 | 箱詰め装置、箱詰め方法 |
| CN114291318B (zh) * | 2022-01-14 | 2022-11-15 | 无锡同联机电工程有限公司 | 一种全自动连续式开封装一体机 |
| CN114313409B (zh) * | 2022-01-25 | 2022-11-11 | 华格电子(昆山)有限公司 | 一种gdt整列包装机 |
| EP4273052A1 (de) * | 2022-03-17 | 2023-11-08 | ISHIDA CO., Ltd. | Schachtelverpackungsvorrichtung |
| JP2023173670A (ja) * | 2022-05-26 | 2023-12-07 | 株式会社デンソーウェーブ | ロボットアームの制御システム |
| CN116022417B (zh) * | 2023-03-30 | 2023-06-06 | 小仙炖霸州食品有限公司 | 一种包装箱码放传送系统 |
| CN116395177A (zh) * | 2023-03-31 | 2023-07-07 | 南通通机股份有限公司 | 一种洗衣皂全自动装箱系统 |
| CN120207678B (zh) * | 2025-05-27 | 2025-08-12 | 四川德合制药有限公司 | 一种药瓶包装贮放容器、打包流水线及打包方法 |
Family Cites Families (21)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4124967A (en) * | 1977-09-19 | 1978-11-14 | Beer Frederick W | Method and apparatus for placing flexible packages in containers |
| DE3417157C2 (de) * | 1984-05-09 | 1986-06-05 | Max Kettner Verpackungsmaschinenfabrik GmbH & Co KG, 8000 München | Vorrichtung zum Umkippen und Anordnen ankommender Kartons in mehreren Reihen auf einen Förderer |
| JPS6164627A (ja) * | 1984-09-03 | 1986-04-03 | エービー テトラパック | 物品集積装置における集積物品の分割装置 |
| DE3720638A1 (de) | 1986-07-22 | 1988-01-28 | Hoefliger Harro Verpackung | Verfahren und vorrichtung zum befuellen von umkartons mit in trays eingestellten, gefuellten tuben |
| DE3641859A1 (de) * | 1986-12-08 | 1988-06-09 | Ficker Otto Ag | Verfahren zum automatischen verpacken von briefhuellen und versandtaschen in ein behaeltnis und verpackungsautomat insbesondere zum durchfuehren der verfahren |
| US4955175A (en) * | 1989-02-06 | 1990-09-11 | Mobil Oil Corporation | Two-stage box pusher for carton indexer |
| US5386677A (en) * | 1991-08-23 | 1995-02-07 | Seibu Electric & Machinery Co., Ltd. | Goods arrangement method and apparatus |
| US5732536A (en) * | 1996-10-28 | 1998-03-31 | Industrial Technology Research Institute | Tape roll in-series package machine |
| US5778640A (en) * | 1996-11-07 | 1998-07-14 | Blueprint Automation, Inc. | Apparatus and method for packing stand-up pouches into cartons |
| US5794417A (en) * | 1997-01-27 | 1998-08-18 | Philip Morris Incorporated | Versatile case packing device |
| DE19821969A1 (de) * | 1998-05-18 | 1999-11-25 | Focke & Co | Vorrichtung zum Verpacken von Gruppen von (Einzel-)Packungen |
| IT1308987B1 (it) * | 1999-01-29 | 2002-01-15 | Futura Srl | Dispositivo di prelevamento e posizionamento di contenitori inconfezioni |
| US6484475B1 (en) * | 1999-02-02 | 2002-11-26 | Kisters Kayat, Inc. | Modular packaging machine |
| DE10130356A1 (de) * | 2001-06-23 | 2003-01-09 | Wiko Piehler Palettier Und Foe | Vorrichtung und Verfahren zum Beladen von Stückgut in einen Behälter |
| US6792741B1 (en) * | 2003-09-08 | 2004-09-21 | Dominic Theriault | Container packing system |
| JP2005306454A (ja) * | 2004-04-23 | 2005-11-04 | Topack Co Ltd | スティック状分包の多段重積機 |
| ITBO20040347A1 (it) * | 2004-05-31 | 2004-08-31 | Packservice S R L | Macchina incartonatrice semiautomatica |
| CN2734694Y (zh) * | 2004-10-28 | 2005-10-19 | 江阴市华夏包装机械有限公司 | 振荡理箱台 |
| NL1032449C2 (nl) * | 2006-09-06 | 2008-03-07 | Robert Bosch Verpakkingsmachin | Inrichting voor het in een doos verpakken van voorwerpen alsmede een dergelijke werkwijze. |
| CN201132614Y (zh) * | 2007-12-03 | 2008-10-15 | 陈顺利 | 马赛克瓷砖全自动收砖铺贴线 |
| US8336700B2 (en) * | 2009-04-08 | 2012-12-25 | Ima North America, Inc. | Transport system for moving a plurality of containers through a plurality of work stations |
-
2011
- 2011-01-12 DE DE102011002575A patent/DE102011002575A1/de not_active Withdrawn
-
2012
- 2012-01-03 EP EP12700061.0A patent/EP2663497B1/de not_active Not-in-force
- 2012-01-03 CN CN201280005157.2A patent/CN103298696B/zh not_active Expired - Fee Related
- 2012-01-03 BR BR112013017599A patent/BR112013017599A2/pt not_active IP Right Cessation
- 2012-01-03 US US13/979,496 patent/US20130283731A1/en not_active Abandoned
- 2012-01-03 WO PCT/EP2012/050030 patent/WO2012095332A1/de not_active Ceased
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US10414528B2 (en) | 2015-05-29 | 2019-09-17 | Graphic Packaging International, Llc | Packaging system |
| US11814199B2 (en) | 2015-05-29 | 2023-11-14 | Graphic Packaging International, Llc | Packaging system |
| US12378023B2 (en) | 2015-05-29 | 2025-08-05 | Graphic Packaging International, Llc | Packaging system |
Also Published As
| Publication number | Publication date |
|---|---|
| DE102011002575A1 (de) | 2012-07-12 |
| EP2663497A1 (de) | 2013-11-20 |
| CN103298696A (zh) | 2013-09-11 |
| WO2012095332A1 (de) | 2012-07-19 |
| US20130283731A1 (en) | 2013-10-31 |
| CN103298696B (zh) | 2016-02-10 |
| BR112013017599A2 (pt) | 2016-10-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| WO2012095332A1 (de) | Verpackungsvorrichtung | |
| EP2254819B1 (de) | Vorrichtung zum stapeln von produktgruppen oder gebinden | |
| EP3266718B1 (de) | Verpackungsmaschine mit einer zwischenablageeinrichtung für verpackte pharmazeutische erzeugnisse | |
| EP0298294A1 (de) | Vorrichtung zum Gruppieren von Packungen | |
| WO2013010697A1 (de) | Anordnung zum bepacken von boxen | |
| DE102019113129B4 (de) | Verpackungsmaschine zum anordnen von elementen, vorzugsweise kartons, auf paletten, und verfahren hierfür | |
| DE2022602C3 (de) | Automatische Verpackungsanlage, insbesondere für Zigaretten, mit mehreren Abgabemaschinen, einer Sammelpackmaschine und einem Zwischenspeicher | |
| CH690712A5 (de) | Verfahren und Vorrichtung zur Abpackung von Dosen oder Tuben. | |
| DE102019102118A1 (de) | Palette zum Transportieren von Abstandshaltern für Zigarettenpackungen | |
| US11117749B2 (en) | Apparatus for handling articles as well as method for exchanging at least one transport module and at least one work module of the apparatus | |
| WO2011066897A1 (de) | Vorrichtung zum handhaben von grosspackungen mit einer mehrzahl von gegenständen als packungsinhalt | |
| DE3424233C2 (de) | ||
| EP1107865B1 (de) | Vorrichtung zum herstellen und abtransportieren von stapeln aus kunststoffbeuteln, insbesondere automatenbeuteln | |
| EP0562446B1 (de) | Einrichtung zum Einführen von (Klein-)Packungen, insbesondere Zigaretten-Packungen, in einen Karton | |
| EP0438714A1 (de) | Verpackungsmaschine mit einer Einrichtung zur Förderung von Verpackungsmaterial in ihrem Bereich | |
| DE102019128197B4 (de) | Depalettieranordnung mit einer Vorrichtung zum Depalettieren von stapelbaren Stückgutgebinden und Verfahren zum Depalettieren von stapelbaren Stückgutgebinden | |
| EP2404831A1 (de) | Verpackungssystem zum Befüllen eines Sammelbehälters mit Artikeln | |
| DE60004521T2 (de) | Verpackungsmaschine und kontrolleinrichtung | |
| EP0977695A1 (de) | Vorrichtung zum sammeln und palettieren von flaschen | |
| EP0566870A1 (de) | Vorrichtung zum Abpacken von gruppierten Einzelpackungen, insbesondere vorverpackten Lebensmittelprodukten, wie Butter, Margarine oder dgl. in einen Umkarton oder dgl. | |
| CH691899A5 (de) | Verfahren und Vorrichtung zum Verpacken von Dosen oder Tuben. | |
| DE29807325U1 (de) | Vorrichtung zum Sammeln und Palettieren von Flaschen | |
| DE2755390C2 (de) | Verfahren und Vorrichtung zur gleichmäßigen Zuführung von Gegenständen zu einer Verarbeitungsmaschine | |
| DE69415328T2 (de) | Verfahren zum bilden gestapelter gruppen von gegenständen in verpackungen | |
| EP4452761A1 (de) | Verpackungsvorrichtung und verpackungsverfahren zum überführen von artikeln in umverpackungen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20130812 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20140722 |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: KOMP, RAINER |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 694463 Country of ref document: AT Kind code of ref document: T Effective date: 20141115 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502012001536 Country of ref document: DE Effective date: 20141218 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150305 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150205 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150305 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150206 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502012001536 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150103 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| 26N | No opposition filed |
Effective date: 20150806 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150131 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150131 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20160103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20120103 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 694463 Country of ref document: AT Kind code of ref document: T Effective date: 20170103 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20180124 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170103 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20180124 Year of fee payment: 7 Ref country code: IT Payment date: 20180126 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141105 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20190201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190201 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190103 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 502012001536 Country of ref document: DE Representative=s name: DAUB, THOMAS, DIPL.-ING., DE Ref country code: DE Ref legal event code: R081 Ref document number: 502012001536 Country of ref document: DE Owner name: SYNTEGON TECHNOLOGY GMBH, DE Free format text: FORMER OWNER: ROBERT BOSCH GMBH, 70469 STUTTGART, DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20210120 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502012001536 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220802 |