EP0634238B1 - Vorrichtung zum Kühlen von Giesserei-Formsand - Google Patents
Vorrichtung zum Kühlen von Giesserei-Formsand Download PDFInfo
- Publication number
- EP0634238B1 EP0634238B1 EP94102687A EP94102687A EP0634238B1 EP 0634238 B1 EP0634238 B1 EP 0634238B1 EP 94102687 A EP94102687 A EP 94102687A EP 94102687 A EP94102687 A EP 94102687A EP 0634238 B1 EP0634238 B1 EP 0634238B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sand
- cooling
- cooling section
- bin
- bunker
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000004576 sand Substances 0.000 title claims abstract description 40
- 238000001816 cooling Methods 0.000 title claims abstract description 26
- 238000000465 moulding Methods 0.000 title claims abstract 5
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims abstract description 11
- 239000000498 cooling water Substances 0.000 claims abstract description 3
- 239000007921 spray Substances 0.000 claims description 7
- 230000001105 regulatory effect Effects 0.000 claims description 6
- 239000000523 sample Substances 0.000 claims description 4
- 238000007599 discharging Methods 0.000 claims 1
- 238000005507 spraying Methods 0.000 abstract 2
- 241000273930 Brevoortia tyrannus Species 0.000 description 9
- 239000003110 molding sand Substances 0.000 description 7
- 238000000034 method Methods 0.000 description 4
- 238000005538 encapsulation Methods 0.000 description 2
- 230000033228 biological regulation Effects 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 238000000605 extraction Methods 0.000 description 1
- 230000014759 maintenance of location Effects 0.000 description 1
- 230000000737 periodic effect Effects 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C5/00—Machines or devices specially designed for dressing or handling the mould material so far as specially adapted for that purpose
- B22C5/08—Machines or devices specially designed for dressing or handling the mould material so far as specially adapted for that purpose by sprinkling, cooling, or drying
Definitions
- the invention is directed to a cooling device of hot foundry sand extracted from a bunker with a cooling section and a spray device for application of cooling water.
- Applicant's 08 538 is a generic device known in the following a molding sand hopper
- a vibratory conveyor is assigned as the conveyor and rinsing section is.
- the vibratory conveyor has an air permeable Floor, a spray device is assigned to it, wherein the conveyor line is encapsulated such that applied Air can discharge steam.
- the vibratory bowl feeder can be switched on or off.
- DE-A-1 947 566 describes a method for regulating the Moisture from molding sand is known in a mixing drum the addition of water depending on the power consumption the mixing drum is regulated. A sand cooling is not provided there.
- the object of the invention is to provide a solution with which is an essentially continuous operation of the cooling device Even with strongly fluctuating sand supply with retention the homogeneity of the chilled sand among fluctuating Operating states is made possible.
- the sprayed Water volume is regulated so that at the end of the cooling section a qualitative under practically all operating conditions same sand can be removed.
- the regulation of the water quantities to be sprayed on can be done by Variations in the pulse-pause ratio of the spray nozzles are set will.
- the extraction device is particularly expedient to use the extraction device as an endless conveyor training with a sand discharge on the cooling section, as it is known in itself, but it is also possible to exit the bunker immediately after the start of the Assign cooling section, whereby between bunker discharge and A controllable discharge roller as the take-off device for the cooling section can be provided.
- control is carried out so that the Current actual value of the speed of the vibratory conveyor drive is converted as a measure of the sand throughput, whereby from the current sand throughput performance with the help the sand temperature in front of, in and / or behind the cooler control of the amount of water required for cooling becomes.
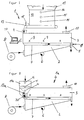
- the device essentially becomes from a vibratory conveyor 2, which is in an encapsulation 3 is housed, formed with a molding sand 4 and a molding sand deduction 5.
- the vibratory conveyor 2 has a drive 6 which, like all device elements in the figures, only hinted at is reproduced.
- the vibrating conveyor trough has one air-permeable bottom 7 through which by means of a blower 8 air is pressed.
- the hot sand on the conveyor trough is sprayed with water vapor from nozzles 9, the air from the blower 8 with the resulting water vapor deducted over the nozzle 10, which is indicated by small arrows is.
- Deduction 12 are in the example shown three level probes 14 to 16 are provided to the respective capture current level and in a symbolic only reproduced process computer 17 feed.
- in the Throw-in area is at least one temperature sensor 18 to determine the feed temperature of the sand and on Deduction 5 is a temperature sensor 19 for determining the delivery temperature of the sand. This data will also be fed to the process computer 17.
- the mode of action is as follows:
- the current speed of the drive is shown on the computer 6 of the vibratory conveyor 2 is detected and from it the funded Amount of sand calculated. Via the temperature sensors 18 and 19 the task and the end temperature are determined, whereby the current level via the level indicators 14 to 16 of the molding sand silo is determined, with the The speed of the trigger element 13 is also recorded as a controlled variable becomes.
- a control in the Way made using a control algorithm with the help e.g. of a frequency converter the speed of the trigger element is changed so that the fill level of the bunker is approximately remains constant.
- the amount of water required for cooling is calculated.
- the metering of the amount of water can be done by relation of the Pulse-pause ratio take place through the opposite the passage time of the sand in the cooler in smaller Periodic spray nozzles 9.
- a cooler according to the invention can e.g. to 80% of the Peak sand performance can be dimensioned without losing it Limit cooling capacity. It is also achieved that the Cooler continuously despite different sand application can be operated, which ensures the homogeneity of the cooled Sandes remains intact because the above described strong leaps and bounds here do not occur.
- Task member 13a which in this device 1a as a feed roller 20 is designed.
- This driven application roller 20 below the 11a designated bunkers within the encapsulation 3 offers a A number of advantages that can occur when the roller is at a standstill no sand runs out of the bunker, there is one lower height, which also ensures that no Rieselsand is created, as is the case with the discharge of belt conveyors is often the case.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
- Mold Materials And Core Materials (AREA)
Description
Claims (4)
- Vorrichtung (1) zur Kühlung von heißem, aus einem Bunker (11) abgezogenen Gießerei-Formsand mit einer Kühlstrecke (2,3) und einer Besprüheinrichtung (9) zum Aufbringen von Kühlwasser,
dadurch gekennzeichnet,
daß dem Bunker (11) ein kontinuierlich leistungsgeregeltes Abzugsorgan (13) zur Beaufschlagung der Kühlstrecke (2,3) mit heißem Gießerei-Formsand und eine Regeleinrichtung (17) zur Dosierung der aufzusprühenden Wassermenge in Abhängigkeit der Leistung des Bunkerabzugsorganes (11) zugeordnet ist, wobei die Regeleinrichtung (17) zur Beeinflussung des Puls-Pausenverhältnisses der Sprüheinrichtung (9) in Abhängigkeit der mittels Meßsonden (18,19) bestimmten Sandaufgabe- bzw. -entnahmetemperatur im Einwurfsbereich (4) bzw. Auswurfsbereich (5) der Kühlstrecke (2,3) ausgebildet ist. - Vorrichtung nach Anspruch 1,
dadurch gekennzeichnet,
daß das Abzugsorgan als Endlosförderer (11) mit einem Sandabwurf auf die Kühlstrecke (2,3) ausgebildet ist. - Vorrichtung nach Anspruch 1,
dadurch gekennzeichnet,
daß der Bunkeraustritt (12) unmittelbar dem Beginn der Kühlstrecke (2,3) zugeordnet ist, wobei zwischen Bunkerauswurf (12) und Kühlstreckenbeginn (4) als Abzugsorgan eine regelbare Auftragswalze (20) vorgesehen ist. - Vorrichtung nach einem der vorangehenden Ansprüche,
dadurch gekennzeichnet,
daß die Kühlstrecke als gekapselter Schwingförderer (2) mit einem luftdurchlässigen Boden (7) ausgebildet ist mit einem Kühllufteintraggebläse (8) unterhalb des Bodens und einem Dampfaustritt (10) am Ende der Kühlstrecke.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE4324101A DE4324101A1 (de) | 1993-07-17 | 1993-07-17 | Vorrichtung zum Kühlen von Gießerei-Formsand |
| DE4324101 | 1993-07-17 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0634238A1 EP0634238A1 (de) | 1995-01-18 |
| EP0634238B1 true EP0634238B1 (de) | 1998-04-08 |
Family
ID=6493134
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP94102687A Expired - Lifetime EP0634238B1 (de) | 1993-07-17 | 1994-02-23 | Vorrichtung zum Kühlen von Giesserei-Formsand |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0634238B1 (de) |
| AT (1) | ATE164789T1 (de) |
| DE (2) | DE4324101A1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102011105800A1 (de) | 2011-06-17 | 2012-12-20 | Jöst GmbH + Co. KG | Verfahren und Vorrichtung zur Aufbereitung von Formsand |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2810852B1 (fr) * | 2000-07-03 | 2004-10-15 | Ate Soc Nouvelle | Conquet a fond vibrant |
| DE10051045C2 (de) † | 2000-10-14 | 2002-11-07 | Amos Maschinenfabrik Und Anlag | Traubenauffangbehälter und Traubentransportfahrzeug |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1133508B (de) * | 1958-05-16 | 1962-07-19 | Pekay Machine & Engineering Co | Vorrichtung zum Befeuchten von Formsand |
| CH359246A (de) * | 1961-07-14 | 1961-12-31 | Fischer Ag Georg | Vorrichtung zum Kühlen von Formsand für Giessereien |
| CH480105A (de) * | 1968-10-07 | 1969-10-31 | Fischer Ag Georg | Verfahren zur Regelung der Feuchtigkeit von körnigen Massen, insbesondere von Formsand und Vorrichtung zur Durchführung des Verfahrens |
| DE3008538C2 (de) * | 1980-03-06 | 1986-01-23 | Uhde Gmbh, 4600 Dortmund | Vorrichtung zum Kühlen von heißem Gießerei-Formsand |
-
1993
- 1993-07-17 DE DE4324101A patent/DE4324101A1/de not_active Withdrawn
-
1994
- 1994-02-23 DE DE59405620T patent/DE59405620D1/de not_active Expired - Lifetime
- 1994-02-23 EP EP94102687A patent/EP0634238B1/de not_active Expired - Lifetime
- 1994-02-23 AT AT94102687T patent/ATE164789T1/de active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102011105800A1 (de) | 2011-06-17 | 2012-12-20 | Jöst GmbH + Co. KG | Verfahren und Vorrichtung zur Aufbereitung von Formsand |
Also Published As
| Publication number | Publication date |
|---|---|
| ATE164789T1 (de) | 1998-04-15 |
| DE4324101A1 (de) | 1995-01-19 |
| EP0634238A1 (de) | 1995-01-18 |
| DE59405620D1 (de) | 1998-05-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2504902C2 (de) | Verfahren und Vorrichtung zum Steuern der Schnittleistung eines Tabakschneiders | |
| CH617002A5 (de) | ||
| DE3202717C2 (de) | ||
| DE2621410C2 (de) | ||
| DE69820319T2 (de) | Vorrichtung zum Ausrichten von Gegenständen | |
| DE2145890A1 (de) | Verfahren zum Vermengen und Homogenisieren von Schüttmaterial sowie Vorrichtung zur Ausführung des Verfahrens | |
| DE3827288C2 (de) | Verfahren und Anordnung zur Durchführung des Verfahrens zum mikrobiologischen Abbau von organischen Abfällen | |
| DE1532066B2 (de) | Anordnung zum fortlaufenden Zusammenführen von verschiedenen Tabakkomponenten | |
| WO2000034557A1 (de) | Mischen von faserkomponenten | |
| DE1901690A1 (de) | Verfahren und Vorrichtung zum Trocknen von Tabak | |
| EP0634238A1 (de) | Vorrichtung zum Kühlen von Giesserei-Formsand | |
| DE3230144C2 (de) | ||
| EP0997184A1 (de) | Vorrichtung zum Fördern und Mischen von Schüttgut | |
| DE3543358A1 (de) | Verfahren und vorrichtung zum vergleichmaessigen der feuchte eines tabakstranges | |
| DE3904853C2 (de) | ||
| DE69013465T2 (de) | Ladevorrichtung zum Speisen einer Karde mit Textilfaservlies grösstmöglicher Gleichmässigkeit. | |
| DE3516909C2 (de) | Zigaretten-Fertigungsmaschine | |
| DE2845640A1 (de) | Verfahren zur gewichtsgeregelten speisung von spinnereimaschinen mit textilfasern | |
| EP1516544B1 (de) | Trocknungsanlage und -verfahren zur Trocknung eines Tabakgutes | |
| DE102013206085A1 (de) | Vorrats- und Transporteinrichtung | |
| EP1917388A1 (de) | Flockenbeschickungssystem. | |
| DE2509720A1 (de) | Verteiler einer zigarettenstrangmaschine | |
| DE1273312B (de) | Verfahren zum Temperieren von Schokolade und aehnlichen Fettmassen sowie Vorrichtungzur Durchfuehrung dieses Verfahrens | |
| DE1507887A1 (de) | Verfahren und Vorrichtung zum Herstellen eines bestimmten Mischungsverhaeltnisses verschiedener Komponenten | |
| CH421907A (de) | Verfahren zur Herstellung von plastischen bis zähflüssigen Massen aus einzelnen Komponenten |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE DE ES FR IT NL PT |
|
| 17P | Request for examination filed |
Effective date: 19950310 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: JOEST GMBH + CO. KG |
|
| 17Q | First examination report despatched |
Effective date: 19970407 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE DE ES FR IT NL PT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19980408 Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19980408 Ref country code: ES Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19980408 |
|
| REF | Corresponds to: |
Ref document number: 164789 Country of ref document: AT Date of ref document: 19980415 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 59405620 Country of ref document: DE Date of ref document: 19980514 |
|
| ITF | It: translation for a ep patent filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19980708 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| EN | Fr: translation not filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990223 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990228 |
|
| 26N | No opposition filed | ||
| BERE | Be: lapsed |
Owner name: JOST G.M.B.H. + CO. K.G. Effective date: 19990228 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20120221 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20120224 Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 59405620 Country of ref document: DE Representative=s name: VON ROHR PATENTANWAELTE PARTNERSCHAFT MBB, DE Ref country code: DE Ref legal event code: R082 Ref document number: 59405620 Country of ref document: DE Representative=s name: VON ROHR PATENTANWAELTE PARTNERSCHAFT, DE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59405620 Country of ref document: DE Effective date: 20130903 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130223 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130903 |