EP1311354B2 - Verfahren zum streckrichten von kaltband sowie regelung des streckgrades - Google Patents
Verfahren zum streckrichten von kaltband sowie regelung des streckgrades Download PDFInfo
- Publication number
- EP1311354B2 EP1311354B2 EP01971833A EP01971833A EP1311354B2 EP 1311354 B2 EP1311354 B2 EP 1311354B2 EP 01971833 A EP01971833 A EP 01971833A EP 01971833 A EP01971833 A EP 01971833A EP 1311354 B2 EP1311354 B2 EP 1311354B2
- Authority
- EP
- European Patent Office
- Prior art keywords
- roller set
- tension
- strip
- rollers
- degree
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 9
- 230000001105 regulatory effect Effects 0.000 title claims 2
- 238000005452 bending Methods 0.000 claims abstract description 13
- 238000009826 distribution Methods 0.000 description 3
- 230000015572 biosynthetic process Effects 0.000 description 2
- 230000001186 cumulative effect Effects 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 229910052751 metal Inorganic materials 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 229910000831 Steel Inorganic materials 0.000 description 1
- 230000002411 adverse Effects 0.000 description 1
- 229910052782 aluminium Inorganic materials 0.000 description 1
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 1
- 230000000295 complement effect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 150000002739 metals Chemical class 0.000 description 1
- 229910001220 stainless steel Inorganic materials 0.000 description 1
- 239000010935 stainless steel Substances 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B37/00—Control devices or methods specially adapted for metal-rolling mills or the work produced thereby
- B21B37/48—Tension control; Compression control
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D1/00—Straightening, restoring form or removing local distortions of sheet metal or specific articles made therefrom; Stretching sheet metal combined with rolling
- B21D1/05—Stretching combined with rolling
Definitions
- the invention relates to a method for stretch straightening of cold strip with the features specified in the independent claims. Such a method is from the US 5,704,237 A known.
- the EP 0 393 301 B2 For example, there has been disclosed a method of continuously drawing metallic strips having a strip thickness of between 0.05 mm and 0.5 mm, particularly bands of steel, aluminum or similar metals. There, the strip to straightening passes through a brake roller and a Switzerlandrollensatz and is subjected to a stretch train between two sets of rollers in the course of his stretching in the plastic range, which corresponds to the yield strength of the strip material or slightly exceeds this yield strength.
- the invention has for its object to provide a generic method by which stretch to straighten, annealed, pickled and optionally dressed cold strips with improved quality, especially a high surface quality, elastic and plastic stretch.
- the band is plastically extended by superposition of tape tension and bending in the casserole or drain point of the tape on the individual roles of the high-tensile roller set. It can thereby achieve a point-symmetrical structure of the bends in the other set of rollers, especially in thicker bands that can not be stretched by pure train between the rollers.
- the tape is passed through the roller set with a short guy length between the respective run-off and run-off points of the individual rollers.
- this short guy length which is understood as the free, unguided length of the tape between two consecutive roles in the tape, the tape is improved and reduces the tendency of the tape to form longitudinal folds.
- the short guy length can be achieved, for example, by the fact that the rollers of the roller set succeeding one another in the direction of the wrap or of the belt pass are spaced less from one another than is the case with conventional S-roll arrangements.
- a preferred measure provides that the degree of stretching is controlled as follows, that in the arranged between the brake and the Werrollensatz further set of rollers the Einzelstreckgrade be summed up in the up and discharge points of the individual roles to a cumulative degree, to which the degree of stretching outside the roller set between in each case building the train and directing or directing and dismantling the train roles of the brake and Werrollensatzes be tapped and returned to the torques of the rollers of the other set of rollers. It is thus no longer between the roles of a differential speed required, which finally results in a required degree of stretch behind two rollers, but can be achieved with this scheme meaningful distributions of the individual degrees of stretch.
- the brake roller set 3 is formed with four rollers 6 and the Werner roller set 5 with four rollers 7 , which are arranged in pairs S-shaped.
- the Hochzug roller set 5 also has four rollers, which also in pairs
- S-shaped are arranged, in each case the inner pull rollers 8a and 9a and the respective complementary rollers 8b and 9b.
- the upper roller pair 8a, 8b and the lower roller pair 9a, 9b is arranged on the one hand with respect to the individual rollers to each other and on the other hand from pair of rollers to pair of rollers in the smallest possible distance. It is thus a short guy length 10, each defined between the run-off point 11 of the preceding in the strip running direction to the roll following in the direction of travel, achieved, whereby the tape improves and the formation of longitudinal folds (towel effect) is reduced. Since the band 2 in the high-tension roller set 5 is subject to a bending deflection-in the case of only one pair of rollers, in any case, a bend-in the high-tension roller set 5, a degree of stretching increased by the bending of the band under tension.
- the resulting due to bending of the belt 2 with superimposed train degree of stretching is in this case the larger, the smaller the diameter of the rollers.
- the limits are where a small roll diameter will adversely affect delicate tape surfaces because a rather large roll diameter, e.g. 800 to 1500 mm, minimizes the influence.
- Whatever the roll diameter are chosen, so in any case creates a plastic extension of the belt 1 by superposition of tape tension and bending in the casserole or drain point 11, 12 of the rollers 8a, 8b and 9a, 9b.
- a Hochzug roller set 5 is arranged as in the example described above between the brake roller 30 and the Werrollensatz 40.
- the brake and the Werrollensatz 30 or 40 here, however, consists of only one of the rollers 6 and 7 formed roller pair, but the roller assembly of the Hochzug roller set 5 turn on the one hand for a short guy length 10 and on the other hand by bending with superimposed train resulting in a high degree of stretching.
- the control scheme shown allows the degree of stretch to be summed up by the mutual influence of the individual degrees of stretch in the up and down points 12 and 11 of the rollers in the high-tension roller set 5 to a cumulative degree. It is achieved with a suitable feedforward control and regulation of the individual torques a desired degree of stretching.
- the degrees of stretching are tapped outside the high-train roller set 5 between the train and directing rollers or the directing and the train-reducing roles of the brake and Werrollensatzes 30 and 40 and returned to the torques of the rollers of the high-tensile roller set 5. It is thus a meaningful distribution of Einzelstreckgrade possible.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Straightening Metal Sheet-Like Bodies (AREA)
- Pinball Game Machines (AREA)
- Heat Treatment Of Strip Materials And Filament Materials (AREA)
- Basic Packing Technique (AREA)
Description
- Die Erfindung betrifft ein Verfahren zum Streckrichten von Kaltband mit den in dem unabhängigen Ansprüch angegebenen Merkmalen. Ein solches Verfahren ist aus der
US 5.704.237 A bekannt. - Weiterhin ist durch die
EP 0 393 301 B2 ist ein Verfahren zum kontinuierlichen Zugrecken von metallischen Bändern mit einer Banddicke zwischen 0,05 mm und 0,5 mm, insbesondere von Bändern aus Stahl, Aluminium oder dergleichen Metallen bekanntgeworden. Dort durchläuft das zu streckrichtende Band einen Bremsrollensatz und einen Zugrollensatz und wird zwischen beiden Rollensätzen im Zuge seiner Reckung im plastischen Bereich einem Streckzug unterworfen, welcher der Streckgrenze des Bandmaterials entspricht oder diese Streckgrenze geringfügig übersteigt. - Damit sich die bei plastischer Reckung auftretenden Bandqueränderungen auf ein Minimum reduzieren und damit die Bildung von Mittenschüsseln sowie von über die Bandbreite ungleichmäßig verteilten Restspannungen nahezu eliminieren lassen, weist diese Streckrichtanlage zwischen dem Brems- und dem Zugrollensatz ein Zugreckrollenpaar auf, so dass das Band mit einem zusätzlichen Streckzug überlagert wird, welcher eine Reckung im plastischen Bereich bewirkt. Während den Rollen des Brems- und des Zugrollensatzes hierbei ein verhältnismäßig hoher Streckzuganteil zukommt, wird mit dem Zugreckrollenpaar nur etwa 5 bis 25 % des Streckzuges erzeugt.
- Der Erfindung liegt die Aufgabe zugrunde, ein gattungsgemäßes Verfahren zu schaffen, mit denen sich die zu streckrichtenden, geglühten, gebeizten und gegebenenfalls dressierten Kaltbänder mit verbesserter Qualität, insbesondere einer hohen Oberflächengüte, elastisch und plastisch strecken lassen.
- Diese Aufgabe wird mit einem Verfahren erfindungsgemäß dadurch gelöst, dass mit dem weiteren Rollensatz der Hauptteil es Streckzuges erzeugt wird. Eine Maßnahme sieht hierzu vor, dass das Band in dem Rollensatz einer Wechselbiegung unterworfen wird. Hiermit wird die Erkenntnis umgesetzt, dass bei einer Biegung des Bandes mit überlagertem Zug der resultierende Streckgrad größer wird und sich auch Banddicken der Bänder, vorrangig aus Edelstahl, aber auch Bänder aus solchen Werkstoffen, die sich durch eine hohe Oberflächengüte auszeichnen, von mehr als 0,5 mm mit einer Erhöhung der erzielbaren Planlage und Reduzierung der Eigenspannungszustände streckrichten lassen. Damit einhergehend wird die Oberflächenfeingestalt und der Oberflächenglanz des streckgerichteten Metallbandes verbessert. Die Betriebsweise mit Wechselbiegung in dem weiteren, erfindungsgemäß den Hauptanteil des Streckzuges erzeugenden Rollensatz, während der verbleibende Streckgrad auf den Brems- und Zugrollensatz verteilt wird, trägt dazu bei, den Streckgrad weiter zu erhöhen.
- Nach dem Vorschlag der Erfindung wird das Band durch Überlagerung von Bandzug und Biegung im Auflauf- bzw. Ablaufpunkt des Bandes auf die einzelnen Rollen des Hochzug-Rollensatzes plastisch verlängert. Es läßt sich hierdurch ein punktsymmetrischer Aufbau der Biegungen in dem weiteren Rollensatz erreichen, insbesondere bei dickeren Bändern, die nicht durch reinen Zug zwischen den Rollen gestreckt werden können.
- Das Band wird mit kurzer 'Abspannlänge zwischen den jeweiligen Ab- und Auflaufpunkten der einzelnen Rollen durch den Rollensatz hindurchgeführt. Durch diese kurze Abspannlänge, worunter die freie, ungeführte Länge des Bandes zwischen zwei im Bandlauf aufeinanderfolgenden Rollen verstanden wird, wird der Bandlauf verbessert und die Neigung des Bandes zur Bildung von Längsfalten vermindert. Die kurze Abspannlänge läßt sich bspw dadurch erreichen, dass die in Richtung der Umschlingung bzw. des Banddurchlaufs aufeinanderfolgenden Rollen des Rollensatzes einen geringeren Abstand voneinander aufweisen, als das bei üblichen S-Rollenanordnungen der Fall ist.
- Eine bevorzugte Maßnahme sieht vor, daß der Streckgrad folgendermaßen geregelt wird, dass in dem zwischen dem Brems- und dem Zugrollensatz angeordneten weiteren Rollensatz die Einzelstreckgrade in den Auf- und Ablaufpunkten der einzelnen Rollen zu einem Summenstreckgrad aufsummiert werden, wozu die Streckgrade außerhalb des Rollensatzes zwischen jeweils den Zug aufbauenden und richtenden bzw. den richtenden und den Zug abbauenden Rollen des Brems- und des Zugrollensatzes abgegriffen und auf die Drehmomente der Rollen des weiteren Rollensatzes zurückgeführt werden. Es wird somit nicht mehr zwischen den Rollen eine Differenzgeschwindigkeit erforderlich, die abschließend hinter zwei Rollen einen geforderten Streckgrad ergibt, vielmehr lassen sich mit dieser Regelung sinnvolle Verteilungen der Einzelstreckgrade erreichen.
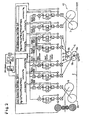
- Weitere Einzelheiten und Vorteile der Erfindung ergeben sich aus den Ansprüchen und der nachfolgenden Beschreibung von in den Zeichnungen dargestellten Ausführungsbeispielen der Erfindung. Es zeigen:
- Figur 1
- in sehr schematischer Seitenansicht eine Ausführung einer Streckrichtanlage mit einem zwischengeschalteten Hochzug-Teil; und
- Figur 2
- ein Regelschema zur Regelung des Streckgrades mit Verteilung der Einzelstreckgrade.
- Eine Anlage 1 zum Streckrichten von Edelstahlbändem 2, vorzugsweise mit Dicken oberhalb 0,5 mm, besteht gemäß
Fig. 1 aus einem Bremsrollensatz 3 und - in Richtung des durch Pfeile gekennzeichneten Banddurchlaufs gesehen sich daran anschließend - einem weiteren, nachfolgend Hochzug-Rollensatz 5 genannten Rollensatz und einem Zugrollensatz 4. Der Bremsrollensatz 3 ist mit vier Rollen 6 und der Zugrollensatz 4 mit vier Rollen 7 ausgebildet, die jeweils paarweise S-förmig angeordnet sind. Der Hochzug-Rollensatz 5 weist ebenfalls vier Rollen auf, die ebenfalls paarweise - S-förmig angeordnet sind, und zwar jeweils die inneren Zugrollen 8a bzw. 9a und die jeweils komplementären Rollen 8b bzw. 9b.
- Das obere Rollenpaar 8a, 8b und das untere Rollenpaar 9a, 9b ist einerseits in bezug auf die einzelnen Rollen zueinander und andererseits von Rollenpaar zu Rollenpaar in einem möglichst geringen Abstand angeordnet. Es wird damit eine kurze Abspannlänge 10, die sich jeweils zwischen dem Ablaufpunkt 11 der in Bandlaufrichtung vorhergehenden zu der in Bandlaufrichtung folgenden Rolle definiert, erreicht, wodurch der Bandlauf verbessert und die Ausbildung von Längsfalten (Handtucheffekt) vermindert wird. Da das Band 2 in dem Hochzug-Rollensatz 5 einer Wechselbiegung - bei nur einem vorhandenen Rollenpaar auf jeden Fall einer Biegung - unterworfen wird, stellt sich in dem Hochzug-Rollensatz 5 ein durch die Biegung des Bandes unter Zug erhöhter Streckgrad ein.
- Der aufgrund von Biegung des Bandes 2 mit überlagertem Zug resultierende Streckgrad wird hierbei um so größer, je kleiner der Durchmesser der Rollen ist. Die Grenzen liegen dort, wo sich ein kleiner Rollendurchmesser nachteilig auf empfindliche Bandoberflächen auswirkt, denn ein eher großer Rollendurchmesser, z.B. 800 bis 1500 mm, setzt die Beeinflussung herab. Wie auch immer die Rollendurchmesser gewählt sind, so entsteht auf jeden Fall eine plastische Verlängerung des Bandes 1 durch Überlagerung von Bandzug und Biegung im Auflauf- bzw. Ablaufpunkt 11, 12 der Rollen 8a, 8b bzw. 9a, 9b.
- Bei dem in
Fig. 2 gezeigten Regelschema zur Regelung des Streckgrades des Bandes 2 ist wie im zuvor beschriebenen Beispiel zwischen dem Bremsrollensatz 30 und dem Zugrollensatz 40 ein Hochzug-Rollensatz 5 angeordnet. Der Brems- und der Zugrollensatz 30 bzw. 40 besteht hier allerdings nur aus einem von den Rollen 6 bzw. 7 gebildeten Rollenpaar, wobei aber die Rollenanordnung des Hochzug-Rollensatzes 5 wiederum einerseits für eine kurze Abspannlänge 10 und andererseits einen durch Biegung mit überlagertem Zug resultierenden hohen Streckgrad sorgt. - Das gezeigte Regelschema erlaubt es, dass sich der Streckgrad durch die gegenseitige Beeinflussung der Einzelstreckgrade in den Auf- und Ablaufpunkten 12 bzw. 11 der Rollen im Hochzug-Rollensatz 5 zu einem Summenstreckgrad aufsummieren. Es wird mit einer geeigneten Vorsteuerung und Regelung der Einzeldrehmomente ein Sollstreckgrad erreicht. Die Streckgrade werden außerhalb des Hochzug-Rollensatzes 5 zwischen den Zug aufbauenden und richtenden Rollen bzw. den richtenden und den Zug abbauenden Rollen des Brems- und des Zugrollensatzes 30 bzw. 40 abgegriffen und auf die Drehmomente der Rollen des Hochzug-Rollensatzes 5 zurückgeführt. Es wird damit eine sinnvolle Verteilung der Einzelstreckgrade möglich.
Claims (2)
- Verfahren zum Richten von Kaltband (2), wobei das Band einen Bremsrollensatz (3, 30) und einen Zugrollensatz (4, 40)durchläuft und zwischen beiden Rollensätzen im Zuge seiner Reckung einem Streckzug unterworfen wird und in einem zwischen dem Bremsrollensatz (3, 30) und dem Zugrollensatz (4, 40) angeordneten weiteren Rollensatz (5) zur Erhöhung des Streckgrades einer Biegung unter Zug unterworfen wird,
dadurch gekennzeichnet,
dass mit dem weiteren Rollensatz (5) der Hauptteil des Streckzuges erzeugt wird, dass das Band (2) durch Überlagerung von Bandzug und Biegung im Auflauf bzw. Ablaufpunkt (12; 11) des Bandes auf die einzelnen Rollen (8a, 8b; 9a, 9b) des Rollensatzes (5) plastisch verlängert wird, wobei
das Band (12) mit kurzer Abspannlänge (10) zwischen den jeweiligen Ab- und Auflaufpunkten (11, 12) der einzelnen Rollen durch den Rollensatz (5) hindurchgeführt wird, wobei
das Band in dem Rollensatz (5) einer Wechselbiegung unterworfen wird. - Verfahren nach Anspruch 1,
dadurch gekennzeichnet,
daß der Streckgrad folgendermaßen geregelt wird, dass in dem zwischen dem Brems- und dem Zugrollensatz (3, 30; 4, 40) angeordneten weiteren Rollensatz (5) die Einzelstreckgrade in Auf- und Ablaufpunkten (11, 12) der einzelnen Rollen des weiteren Rollensatzes (5) zu einem Summenstreckgrad aufsummiert werden, wozu die Streckgrade außerhalb des Rollensatzes (5) zwischen jeweils den Zug aufbauenden und richtenden bzw. den richtenden und den Zug abbauenden Rollen des Brems- und des Zugrollensatzes (3, 30; 4, 40) abgegriffen und auf die Drehmomente der Rollen (8a, 8b; 9a, 9b) des weiteren Rollensatzes (5) zurückgeführt werden.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10041563A DE10041563A1 (de) | 2000-08-24 | 2000-08-24 | Verfahren und Vorrichtung zum Streckrichten von Kaltband sowie Regelung des Streckgrades |
| DE10041563 | 2000-08-24 | ||
| PCT/EP2001/008873 WO2002016057A1 (de) | 2000-08-24 | 2001-08-01 | Verfahren und vorrichtung zum streckrichten von kaltband sowie regelung des streckgrades |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1311354A1 EP1311354A1 (de) | 2003-05-21 |
| EP1311354B1 EP1311354B1 (de) | 2005-03-16 |
| EP1311354B2 true EP1311354B2 (de) | 2010-07-14 |
Family
ID=7653629
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01971833A Expired - Lifetime EP1311354B2 (de) | 2000-08-24 | 2001-08-01 | Verfahren zum streckrichten von kaltband sowie regelung des streckgrades |
Country Status (11)
| Country | Link |
|---|---|
| US (1) | US6925845B2 (de) |
| EP (1) | EP1311354B2 (de) |
| JP (1) | JP2004506517A (de) |
| KR (1) | KR100845929B1 (de) |
| AT (1) | ATE290932T1 (de) |
| BR (1) | BR0113480A (de) |
| CA (1) | CA2420353C (de) |
| DE (2) | DE10041563A1 (de) |
| ES (1) | ES2239160T5 (de) |
| RU (1) | RU2275263C2 (de) |
| WO (1) | WO2002016057A1 (de) |
Families Citing this family (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ATE381394T1 (de) * | 2001-02-07 | 2008-01-15 | Sms Demag Ag | Vorrichtung zur verbesserung der planheit von gewalztem band, insbesondere von stahlband |
| DE10323811A1 (de) * | 2003-05-23 | 2005-01-13 | Bwg Bergwerk- Und Walzwerk-Maschinenbau Gmbh | Verfahren zum kontinuierlichen Zugrecken von metallischen Bändern und Zugreckanlage |
| DE102004048658A1 (de) * | 2004-10-06 | 2006-04-20 | Sms Demag Ag | Vorrichtung zum kontinuierlichen Zugrecken eines Metallbandes und Verfahren zum Betreiben einer solchen Vorrichtung |
| DE102007006810B3 (de) * | 2007-02-07 | 2008-10-02 | Bwg Bergwerk- Und Walzwerk-Maschinenbau Gmbh | Vorrichtung zum Planieren von Metallbändern |
| DE102008024013B3 (de) | 2008-05-16 | 2009-08-20 | Bwg Bergwerk- Und Walzwerk-Maschinenbau Gmbh | Verfahren und Vorrichtung zum Richten eines Metallbandes |
| RU2390396C1 (ru) * | 2008-08-28 | 2010-05-27 | Открытое акционерное общество "Магнитогорский металлургический комбинат" | Устройство для правки широких горячекатаных полос и способ их правки |
| US9221088B2 (en) * | 2009-04-21 | 2015-12-29 | Fairmont Technologies, Llc | Stretch roll forming |
| RU2465084C2 (ru) * | 2010-11-13 | 2012-10-27 | Открытое акционерное общество "Северский трубный завод" | Способ изготовления труб на непрерывных трубосварочных агрегатах |
| DE102013106243C5 (de) * | 2013-06-14 | 2018-10-04 | Bwg Bergwerk- Und Walzwerk-Maschinenbau Gmbh | Verfahren und Vorrichtung zum Streckbiegerichten von Metallbändern |
| CN103785694B (zh) * | 2013-11-22 | 2016-06-01 | 首钢总公司 | 预防启车断带的方法 |
| KR101518635B1 (ko) * | 2013-12-24 | 2015-05-07 | 주식회사 포스코 | 판재교정장치 및 판재교정방법 |
| US10363590B2 (en) | 2015-03-19 | 2019-07-30 | Machine Concepts, Inc. | Shape correction leveler drive systems |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2529899C3 (de) † | 1975-07-04 | 1980-05-08 | Erwin Kampf Gmbh & Co Maschinenfabrik, 5276 Wiehl | Spannvorrichtung für kontinuierlich durchlaufende Metallbänder |
| DE19509067A1 (de) † | 1995-03-14 | 1996-09-19 | Bwg Bergwerk Walzwerk | Verfahren zum kontinuierlichen Richten von dünnen Metallbändern, insbesondere von Aluminium- und Edelstahl-Bändern mit Banddicken von 0,1 mm bis 0,5 mm, und Richtanlage zur Durchführung des Verfahrens |
| EP0936954B1 (de) † | 1996-11-06 | 2000-07-26 | Kampf GmbH & Co. Maschinenfabrik | Vorrichtung zum zugrecken von dünnen metallbändern |
| EP1029819A2 (de) † | 1999-02-15 | 2000-08-23 | Sumitomo Heavy Industries, Ltd. | Verfahren und Vorrichtung zum Nivellieren einer Bahn |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2526296A (en) * | 1943-08-12 | 1950-10-17 | United Eng Foundry Co | Method and apparatus for processing strip metal |
| US3374653A (en) * | 1965-05-28 | 1968-03-26 | Kaiser Aluminium Chem Corp | Strip leveling apparatus |
| DE2350503B1 (de) * | 1973-10-08 | 1975-01-23 | Bwg Bergwerk Walzwerk | Verfahren und Vorrichtung zum Entzundern und Planieren von Blechbaendern |
| DE3912676A1 (de) * | 1989-04-18 | 1990-10-25 | Bwg Bergwerk Walzwerk | Verfahren und vorrichtung zum kontinuierlichen zugrecken von duennen baendern, insbesondere von metallischen baendern |
-
2000
- 2000-08-24 DE DE10041563A patent/DE10041563A1/de not_active Withdrawn
-
2001
- 2001-08-01 WO PCT/EP2001/008873 patent/WO2002016057A1/de not_active Ceased
- 2001-08-01 ES ES01971833T patent/ES2239160T5/es not_active Expired - Lifetime
- 2001-08-01 AT AT01971833T patent/ATE290932T1/de active
- 2001-08-01 BR BR0113480-9A patent/BR0113480A/pt not_active IP Right Cessation
- 2001-08-01 CA CA002420353A patent/CA2420353C/en not_active Expired - Fee Related
- 2001-08-01 DE DE50105633T patent/DE50105633D1/de not_active Expired - Lifetime
- 2001-08-01 JP JP2002520969A patent/JP2004506517A/ja not_active Withdrawn
- 2001-08-01 KR KR1020037002576A patent/KR100845929B1/ko not_active Expired - Fee Related
- 2001-08-01 RU RU2003107847/02A patent/RU2275263C2/ru not_active IP Right Cessation
- 2001-08-01 US US10/362,488 patent/US6925845B2/en not_active Expired - Fee Related
- 2001-08-01 EP EP01971833A patent/EP1311354B2/de not_active Expired - Lifetime
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2529899C3 (de) † | 1975-07-04 | 1980-05-08 | Erwin Kampf Gmbh & Co Maschinenfabrik, 5276 Wiehl | Spannvorrichtung für kontinuierlich durchlaufende Metallbänder |
| DE19509067A1 (de) † | 1995-03-14 | 1996-09-19 | Bwg Bergwerk Walzwerk | Verfahren zum kontinuierlichen Richten von dünnen Metallbändern, insbesondere von Aluminium- und Edelstahl-Bändern mit Banddicken von 0,1 mm bis 0,5 mm, und Richtanlage zur Durchführung des Verfahrens |
| EP0936954B1 (de) † | 1996-11-06 | 2000-07-26 | Kampf GmbH & Co. Maschinenfabrik | Vorrichtung zum zugrecken von dünnen metallbändern |
| EP1029819A2 (de) † | 1999-02-15 | 2000-08-23 | Sumitomo Heavy Industries, Ltd. | Verfahren und Vorrichtung zum Nivellieren einer Bahn |
Non-Patent Citations (2)
| Title |
|---|
| AUSZUGSWEISE ARTIKEL "ZUR KONZEPTION VON STRECKBIEGERICHTANLAGEN UNTER BEACHTUNG DER PROZESSANFORDERUNGEN", VON A.L. NOÉ, NEUE HÜTTE, 37. JAHRGANG, HEFT 6/7-92, JUNI/JULI 1992, pages 1, 4, 5 † |
| AUSZUSGWEISE BWG-PROSPEKT "BANDPROZESSLINIEN", SEITEN 50 UND 51 MIT DECKBLATT UND ENDBLATT, 7/1992 † |
Also Published As
| Publication number | Publication date |
|---|---|
| RU2275263C2 (ru) | 2006-04-27 |
| WO2002016057A1 (de) | 2002-02-28 |
| DE10041563A1 (de) | 2002-03-07 |
| DE50105633D1 (de) | 2005-04-21 |
| US6925845B2 (en) | 2005-08-09 |
| ATE290932T1 (de) | 2005-04-15 |
| EP1311354A1 (de) | 2003-05-21 |
| ES2239160T5 (es) | 2010-12-02 |
| CA2420353A1 (en) | 2003-02-24 |
| KR20030060879A (ko) | 2003-07-16 |
| US20040020258A1 (en) | 2004-02-05 |
| CA2420353C (en) | 2009-12-22 |
| KR100845929B1 (ko) | 2008-07-11 |
| JP2004506517A (ja) | 2004-03-04 |
| ES2239160T3 (es) | 2005-09-16 |
| EP1311354B1 (de) | 2005-03-16 |
| BR0113480A (pt) | 2003-07-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2119514B1 (de) | Verfahren Richten eines Metallbandes | |
| DE19520541C2 (de) | Verfahren und Vorrichtung zum Korrigieren eines gewalzten, in der Bandebene horizontal gebogenen Metallbandes, insbesondere eines Metallbandes mit einer Banddicke von 0,5 mm bis 2,0 mm | |
| EP1311354B1 (de) | Verfahren und vorrichtung zum streckrichten von kaltband sowie regelung des streckgrades | |
| DE102010024714B4 (de) | Verfahren zum Streckbiegerichten von Metallbändern und Streckbiegerichtanlage | |
| EP0393301A2 (de) | Verfahren und Vorrichtung zum kontinuierlichen Zugrecken von dünnen Bändern, insbesondere von metallischen Bändern | |
| DE102012103366A1 (de) | Verfahren und Vorrichtung zum Zunderbrechen eines zunderbehafteten Metallbandes | |
| DE4230243C1 (de) | Rollensatz für die S-förmige Umlenkung zu planierender dünner Metallbänder | |
| DE1140891B (de) | Verfahren zum Richten von Metallband | |
| DE3636707C2 (de) | ||
| DE102006048427B3 (de) | Walzanlage, nachgerüstete Walzanlage, Walzwerk oder Walzstraße, Verfahren zum Ansteuern einer Walzanlage und Verwendung eines ersten Gerüsts einer Walzanlage | |
| AT389654B (de) | Verfahren und spannvorrichtung zum kontinuierlichen richten von insbesondere duennen metallbaendern | |
| EP3941655B1 (de) | Anlage und verfahren zur herstellung von metallischem warmband | |
| EP0470512B1 (de) | Verfahren zum Richten von Metallbändern im Durchlauf | |
| EP1479460B1 (de) | Verfahren zum kontinuierlichen Zugrecken von metallischen Bändern und Zugreckanlage | |
| EP0008625A1 (de) | Verfahren zum mit einer Durchmesserabnahme einhergehendem Verlängern von warmgewalztem, einen Ausgangsdurchmesser da bis bspw 20 mm aufweisendem Runddraht von 0,1 bis 1% Kohlenstoffgehalt durch HochgradKaltumformen und Einrichtung zur Durchführung des Verfahren | |
| EP1025918A2 (de) | Verfahren und Anlage zum Umformen von Metallband | |
| EP0845310A1 (de) | Drahtkühlung | |
| DE2659318A1 (de) | Verfahren zum walzen von rundstahl | |
| EP0925850A2 (de) | Walzverfahren für ein Metallband | |
| DE1602468C3 (de) | Verfahren und Vorrichtung zum Wechselbiegerichten von Blechen | |
| WO2018082943A1 (de) | Verfahren und anlage zur herstellung eines metallischen bandes | |
| DE202017101090U1 (de) | Biegerichtmaschine zum Biegerichten eines metallischen Flachprodukts | |
| DD145233A1 (de) | Verfahren zum umformen von walzgut | |
| DE1034573B (de) | Vorrichtung zum kontinuierlichen Entzundern von bandartigen Erzeugnissen | |
| DE2134405C3 (de) | Verfahren und Vorrichtung zum Reduzieren von Blechbändern in Bandstraßen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20030117 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050316 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50105633 Country of ref document: DE Date of ref document: 20050421 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050616 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050616 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050801 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20050711 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050831 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050831 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050907 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2239160 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| 26 | Opposition filed |
Opponent name: BWG BERGWERK- UND WALZWERK-MASCHINENBAU GMBH Effective date: 20051121 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| NLR1 | Nl: opposition has been filed with the epo |
Opponent name: BWG BERGWERK- UND WALZWERK-MASCHINENBAU GMBH |
|
| ET | Fr: translation filed | ||
| R26 | Opposition filed (corrected) |
Opponent name: BWG BERGWERK- UND WALZWERK-MASCHINENBAU GMBH Effective date: 20051121 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PLAF | Information modified related to communication of a notice of opposition and request to file observations + time limit |
Free format text: ORIGINAL CODE: EPIDOSCOBS2 |
|
| NLR1 | Nl: opposition has been filed with the epo |
Opponent name: BWG BERGWERK- UND WALZWERK-MASCHINENBAU GMBH |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PLCK | Communication despatched that opposition was rejected |
Free format text: ORIGINAL CODE: EPIDOSNREJ1 |
|
| APAH | Appeal reference modified |
Free format text: ORIGINAL CODE: EPIDOSCREFNO |
|
| APBP | Date of receipt of notice of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA2O |
|
| APBQ | Date of receipt of statement of grounds of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA3O |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: SMS SIEMAG AG |
|
| NLT2 | Nl: modifications (of names), taken from the european patent patent bulletin |
Owner name: SMS SIEMAG AG Effective date: 20090617 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20090813 Year of fee payment: 9 Ref country code: NL Payment date: 20090814 Year of fee payment: 9 Ref country code: FI Payment date: 20090814 Year of fee payment: 9 |
|
| APBU | Appeal procedure closed |
Free format text: ORIGINAL CODE: EPIDOSNNOA9O |
|
| RTI2 | Title (correction) |
Free format text: METHOD FOR TENSION LEVELLING A COLD-ROLLED STRIP AND REGULATING THE DEGREE OF LEVELLING |
|
| PUAH | Patent maintained in amended form |
Free format text: ORIGINAL CODE: 0009272 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT MAINTAINED AS AMENDED |
|
| 27A | Patent maintained in amended form |
Effective date: 20100714 |
|
| AK | Designated contracting states |
Kind code of ref document: B2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: RPEO |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: TD Effective date: 20100906 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: DC2A Effective date: 20101122 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20100728 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20110301 |
|
| EUG | Se: european patent has lapsed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110301 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100801 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20110201 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20110128 Year of fee payment: 10 Ref country code: ES Payment date: 20110128 Year of fee payment: 10 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20110801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100802 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20121207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110802 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110801 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 50105633 Country of ref document: DE Representative=s name: HEMMERICH & KOLLEGEN, DE Ref country code: DE Ref legal event code: R082 Ref document number: 50105633 Country of ref document: DE Representative=s name: HEMMERICH, MUELLER & PARTNER, DE Ref country code: DE Ref legal event code: R081 Ref document number: 50105633 Country of ref document: DE Owner name: SMS GROUP GMBH, DE Free format text: FORMER OWNER: SMS SIEMAG AKTIENGESELLSCHAFT, 40237 DUESSELDORF, DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 50105633 Country of ref document: DE Representative=s name: HEMMERICH & KOLLEGEN PATENTANWAELTE, DE Ref country code: DE Ref legal event code: R082 Ref document number: 50105633 Country of ref document: DE Representative=s name: HEMMERICH & KOLLEGEN, DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20200819 Year of fee payment: 20 Ref country code: FR Payment date: 20200821 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20200826 Year of fee payment: 20 Ref country code: AT Payment date: 20200820 Year of fee payment: 20 Ref country code: BE Payment date: 20200826 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 50105633 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MK Effective date: 20210801 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK07 Ref document number: 290932 Country of ref document: AT Kind code of ref document: T Effective date: 20210801 |