EP0290747B1 - Abfüllstation für eine Kartuschen-Füll- und Verschliess-Maschine - Google Patents
Abfüllstation für eine Kartuschen-Füll- und Verschliess-Maschine Download PDFInfo
- Publication number
- EP0290747B1 EP0290747B1 EP88104073A EP88104073A EP0290747B1 EP 0290747 B1 EP0290747 B1 EP 0290747B1 EP 88104073 A EP88104073 A EP 88104073A EP 88104073 A EP88104073 A EP 88104073A EP 0290747 B1 EP0290747 B1 EP 0290747B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cartridge
- filling
- positioning
- cartridges
- centering device
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000000463 material Substances 0.000 claims abstract description 10
- 235000011837 pasties Nutrition 0.000 claims abstract description 10
- 238000006073 displacement reaction Methods 0.000 claims abstract description 5
- 238000007789 sealing Methods 0.000 claims abstract description 3
- 239000000945 filler Substances 0.000 claims abstract 8
- 238000000034 method Methods 0.000 description 4
- 230000009969 flowable effect Effects 0.000 description 3
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 238000004049 embossing Methods 0.000 description 1
- 238000005429 filling process Methods 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 238000013022 venting Methods 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/42—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation
- B65B43/54—Means for supporting containers or receptacles during the filling operation
Definitions
- the invention relates to a filling station according to the preamble of claim 1.
- the cartridge is supported on a carriage which can be displaced vertically by means of a pneumatically actuated piston-cylinder drive and is pushed over a filling valve which is also arranged vertically and is open at the bottom.
- the circular cylindrical cartridge lies on the slide against a partially circular system. The cartridge itself is not held on the carriage, so that - especially with thin-walled cartridges - their deformation cannot be ruled out with certainty.
- a holding and centering device for cartridges to be filled is known, which are transferred by means of this device from a horizontal delivery position by pivoting into a vertical filling and closing position.
- This holding and centering device has vacuum bores connected to a suction line, by means of which the cartridges are held by vacuum during this transfer process. The cartridge is no longer held in this device while the cartridges are being filled.
- Filling stations for cartridges are also known, in which the respective cartridge is held during filling by means of a holding and centering device which grips the cartridge from below with holding fingers. It is pressed into this device from above by means of a spring lever or a pneumatic cylinder.
- a spring lever When using a spring lever, the holder of the cartridge is not sufficiently firm, so that the cartridge can slip when the cartridge is moved over the filling valve.
- the cartridge is pressed by means of a pneumatic cylinder, the thin-walled cartridge can be deformed, so that proper filling cannot be guaranteed.
- the invention is therefore based on the object of designing a filling station of the generic type in such a way that an exactly centered position of the cartridge before the introduction of the filling valve into the cartridge and a reliable holder which does not deform the cartridge before and during filling is ensured.
- the essence of the invention is that the cartridge is drawn into the holding and centering device by means of the at least one vacuum suction holder.
- the cartridge is therefore only loaded from one side with holding forces, so it is not compressed and thus deformed.
- an absolutely safe centering is guaranteed, since the cartridge cannot change its position relative to the system.
- the cartridge is already gripped by the suction hose or the suction hoses during the feeding in the direction of the system, which then pulls the cartridge onto the contact surface, i.e. shorten while centering the cartridge.
- the further embodiment according to claim 4 enables a particularly simple method of filling valve and centered cartridge relative to each other.
- the cartridges are usually transported and filled in a horizontal position, i.e. the filling valve also has a horizontal position. If, on the other hand, only viscous but still flowable materials are to be filled, then the cartridges must be transported and filled vertically or at least in a position that is still clearly inclined from the horizontal to the vertical.
- the filling station according to the invention can be used in all cases. In the event that the cartridges are transported in the horizontal position of their central longitudinal axes, claims 5 and 6 provide a simple possibility of lifting the cartridge from its lower rest position to the holding and centering device.
- a system for filling and closing cartridges with non-flowable pasty goods essentially consists of a press 1 and a cartridge filling and closing machine 2.
- the press 1 has a vertically standing frame-shaped frame 3, the lower support carrier 4 for a pasty Has well-containing container 5.
- a pressure plate 6 is arranged, which can be pressed into the container 5 by a hydraulically actuated working cylinder 7.
- This working cylinder 7 is supported on an upper crosshead 8 of the frame 3.
- the pasty material is pressed out of the latter into a transport line 9, through which it is fed to a metering device 10 assigned to the machine 2.
- the pasty material is fed in portions in a precisely metered amount to a filling station 11 to be described in more detail below.
- the cartridge filling and closing machine 2 essentially has an elongated machine frame 12, on the one of which - in FIGS. 1 and 2 on the left-hand side in each case - a cartridge magazine 13 is attached.
- the step-by-step transport of cartridges 14 from the magazine 13 via various workstations is carried out by means of a so-called rake 15.
- This is about it is a carriage 16 mounted in the machine frame 12, which can be moved in the working direction 18 and counter to this working direction by means of a pneumatically actuated piston-cylinder drive 17, in each case by the dimension s of a working step.
- prismatic supports 23 are provided for the cartridges 14, between which the transport plate 21 with the drivers 22 of the rake 15 is arranged.
- a cartridge 14 is located in each pair of supports 23 during operation. In this position, the transport plate 21 is located somewhat below the supports 23.
- the drives 19 are first acted upon in the vertical direction, so that the cartridges 14 are lifted out of the supports 23 upwards. Then the drive 17 is acted upon in such a way that it moves the entire slide 16 with the rake 15 in the working direction 18 by the dimension s.
- the drives 19 are acted on in such a way that the transport plate 21 with the drivers 22, that is to say the rake 15, is lowered downward, so that all the cartridges 14 are again placed in supports 23.
- the rake 15 is lowered so far that the driver 22 freely to the bottom of the cartridges lying in the pads 23 14 are.
- the rake is then returned to its starting position.
- This method of raking 15 on a roughly rectangular path when viewed from the side means that the cartridges can always be transported one working step in the direction of work 18.
- the workstations mentioned are a closing station 24 and optionally an embossing station 25, in which an impression is made on the cartridges 14.
- the closed cartridges 14 leave the machine 2 at the end opposite the magazine 13 via a discharge ramp 26.
- the closing station 24 is preceded by a sorting device 27 for pistons for closing the cartridges 14.
- the filling station 11 has a tubular filling valve 28 in its outer shape, the central longitudinal axis 29 of which runs parallel to the central longitudinal axes 30 of the cartridges 14 lying on the supports 23.
- the outer diameter D of the filling valve 28 is somewhat smaller than the inner diameter d of the cartridges 14, so that they can be pushed completely over the filling valve 28 for filling with pasty material.
- the machine frame 12 is covered on its upper side by means of two cover plates 31, 32 which support the supports 23 on their mutually facing edges and between which the rake 15 is arranged.
- Both the filling station 11 associated supports 23 are each associated with a lifting device 33 which has a lifting drive 34 designed as a piston-cylinder drive, the cylinder 35 of which is attached to the underside of the cover plate 31 and 32, respectively.
- a receptacle 37 is attached to each piston rod 36, by means of which the corresponding cartridge 14 can be gripped from below.
- the cartridge 14 located in the associated supports 23 can thus be lifted out of these supports 23 by appropriate pneumatic action on the lifting drives 34 and transported upwards to a holding and centering device 38 for the cartridge located above. In this upper position, the cartridge 14 is shown in broken lines in FIG. 5.
- This holding and centering device 38 has a cylindrical section-shaped system 39 adapted to the shape of the cartridge, in which the cylindrical, thin-walled and easily deformable cartridge 14 is centered such that its axis 30 is aligned with the axis 29 of the filling valve 28.
- the cartridge 14 is held in the system 39 by means of two vacuum suction holders 41, only one of which is shown on the left in FIG. 5.
- These vacuum suction holders 41 each have a bellows-type suction hose 42, the lower open end 43 of which protrudes beyond the cylindrical section-shaped contact surfaces 43 of the system 39.
- a swivel lever 46 is arranged in the system 39 and is lifted by the cartridge 14 when it is drawn into the system 39. In the centered position of the cartridge 14 in the system 39, the pivoting lever is pivoted all the way up and thereby actuates a signal transmitter 47 which triggers a sequential control.
- the holding and centering device 38 is attached to a tubular slide 48 which is arranged on a guide rod 49 so as to be displaceable parallel to the central longitudinal axes 29, 30.
- the guide rod 49 is fixedly attached to the frame 50 of the filling station 11, which in turn is attached to the machine frame 12.
- a displacement drive 51 designed as a pneumatically actuated piston-cylinder drive, is provided, the cylinder 52 of which is attached to the frame 50, while the piston rod 53 is connected to the slide 48.
- the signal transmitter 47 emits a signal by pivoting the pivot lever 46 up
- the cylinder 52 of the displacement drive 51 is acted upon by compressed air in such a way that the piston rod 53 is drawn into it, as a result of which the carriage 48 with the holding and centering device 38 is moved in this way - in FIGS. 4 and 5 to the left that the cartridge 14 located in the device 38 is pushed over the filling valve 28.
- the cylinder 52 is then relieved of pressure.
- the filling of the cartridge 14 begins, in that the metering device 10 presses a corresponding amount of pasty material through the filling valve 28 into the cartridge.
- the cartridge 14 is pushed down from the filling valve 28 in accordance with the degree of its filling, ie the holding and centering device 38 is moved together with the slide 48 in the opposite direction, whereby the piston rod 53 is pulled out of the cylinder 52 of the displacement drive 51 .
- the cylinder 52 is still pressurized with compressed air in the direction of extension of the piston rod 53, so that the slide 48 with the device 38 and the filled cartridge 14 is returned to the starting position in which the cartridge 14 is free from the filling valve 28.
- the cartridge is then lowered into the supports 23 by venting the suction hoses 42 of the vacuum suction holder 41.
- the lifting drives 34 are acted on so that the cartridge 14 is lowered and placed in the supports 23 again.
- the cartridge is then transported one step further by means of the rake 15 in the manner already described, so that it comes into the closing station 24.
- control processes are controlled on the one hand by a control panel 54 attached to the machine frame 12 and on the other hand by a central control device 55.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Basic Packing Technique (AREA)
- Vacuum Packaging (AREA)
Description
- Die Erfindung betrifft eine Abfüllstation nach dem Oberbegriff des Anspruches 1.
- Bei einer derartigen aus der US-A-3 115 906 bekannten Abfüllstation wird die Kartusche auf einem vertikal mittels eines pneumatisch beaufschlagbaren Kolben-Zylinder-Antriebs verschiebbaren Schlitten abgestützt und über ein ebenfalls senkrecht angeordnetes, nach unten offenes Abfüllventil geschoben. Auf dem Schlitten liegt die kreiszylindrische Kartusche gegen eine teilkreisylindrische Anlage an. Die Kartusche selber ist auf dem Schlitten nicht gehalten, so daß - insbesondere bei dünnwandigen Kartuschen - deren Verformung nicht mit Sicherheit ausgeschlossen werden kann.
- Aus der GB-A-2 022 553 ist eine Halte- und Zentriervorrichtung für zu füllende Kartuschen bekannt, die mittels dieser Vorrichtung von einer horizontalen Anlieferungsposition durch Verschwenken in eine vertikale Füll- und Verschlußposition übergeben werden. Diese Halte- und Zentriervorrichtung weist an eine Saugleitung angeschlossene Vakuumbohrungen auf, mittels derer die Kartuschen während dieses Umsetzvorganges durch Vakuum gehalten werden. Während des Befüllens der Kartuschen wird die Kartusche nicht mehr in dieser Vorrichtung gehalten.
- Weiterhin sind Abfüllstationen für Kartuschen bekannt, in denen die jeweilige Kartusche während des Füllens mittels einer Halte- und Zentrier-Vorrichtung gehalten wird, die die Kartusche von unten mit Haltefingern umgreift. Sie wird hierbei von oben mittels eines Federhebels oder eines Pneumatikzylinders in diese Vorrichtung gedrückt. Bei Einsatz eines Federhebels ist die Halterung der Kartusche nicht ausreichend fest, so daß beim Verschieben der Kartusche über das Abfüllventil erstere verrutschen kann. Beim Andrücken der Kartusche mittels eines Pneumatikzylinders kann dagegen die dünnwandige Kartusche verformt werden, so daß ein einwandfreies Füllen nicht gewährleistet ist.
- Der Erfindung liegt daher die Aufgabe zugrunde, eine Abfüllstation der gattungsgemäßen Art so auszugestalten, daß eine exakt zentrierte Lage der Kartusche vor dem Einführen des Abfüllventils in die Kartusche und eine zuverlässige, die Kartusche nicht verformende Halterung vor und während des Abfüllens gewährleistet ist.
- Diese Aufgabe wird erfindungsgemäß durch die Merkmale im Kennzeichnungsteil des Anspruches 1 gelöst. Der Kern der Erfindung liegt darin, daß die Kartusche mittels des mindestens einen Vakuum-Saughalters in die Halte- und Zentrier-Vorrichtung hineingezogen wird. Die Kartusche wird also nur von einer Seite her mit Haltekräften belastet, wird also nicht zusammengedrückt und damit verformt. Außerdem ist eine absolut sichere Zentrierung gewährleistet, da die Kartusche ihre Lage relativ zur Anlage nicht ändern kann. Die Kartusche wird bei der Zuführung in Richtung auf die Anlage bereits von dem Saugschlauch bzw. den Saugschläuchen ergriffen, die sich dann unter Heranziehen der Kartusche an die Anlagefläche, d.h. unter Zentrieren der Kartusche verkürzen.
- Einer sicheren Zentrierung der Kartusche dienen weiterhin die an sich bekannten Weiterbildungen nach den Ansprüchen 2 bzw. 3.
- Die weitere Ausgestaltung nach Anspruch 4 ermöglicht ein besonders einfaches Verfahren von Abfüllventil und zentrierter Kartusche relativ zueinander.
- Wenn pastöses, also nicht mehr fließfähiges Material in die Kartuschen abgefüllt werden soll, dann werden die Kartuschen üblicherweise in horizontaler Lage transportiert und gefüllt, d.h. auch das Abfüllventil hat eine horizontale Lage. Wenn dagegen nur zähe aber noch fließfähige Materialien abgefüllt werden sollen, dann müssen die Kartuschen vertikal oder zumindest in einer aus der horizontalen noch deutlich zur vertikalen hin geneigten Lage transportiert und gefüllt werden. In allen Fällen ist die erfindungsgemäße Abfüllstation einsetzbar. Für den Fall eines Transports der Kartuschen in horizontaler Lage ihrer Mittel-Längs-Achsen geben die Ansprüche 5 und 6 eine einfache Möglichkeit wieder, die Kartusche aus ihrer unteren Ruhelage zur Halte- und Zentrier-Vorrichtung anzuheben.
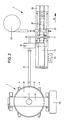
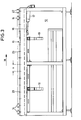
- Die Erfindung wird mit der nachfolgenden Beschreibung eines Ausführungsbeispiels anhand der Zeichnung näher erläutert. Es zeigt
- Fig. 1
- eine vertikale Längs-Ansicht einer Anlage zum Füllen und Verschließen von Kartuschen mit pastösem Material,
- Fig. 2
- eine Draufsicht auf die Anlage nach Fig. 1,
- Fig. 3
- eine vertikale Seitenansicht eines Gestells einer Kartuschen-Füll- und Verschließ-Maschine aus der Anlage nach den Fig. 1 und 2,
- Fig. 4
- eine Seiten-Ansicht einer Abfüllstation der Kartuschen-Füll- und Verschließ-Maschine und
- Fig. 5
- einen Teilausschnitt aus Fig. 4 in gegenüber Fig. 4 vergrößertem Maßstab.
- Eine Anlage zum Füllen und Verschließen von Kartuschen mit nichtfließfähigen pastösen Gütern besteht im wesentlichen aus einer Presse 1 und einer Kartuschen-Füll- und Verschließ-Maschine 2. Die Presse 1 weist ein vertikal stehendes rahmenförmiges Gestell 3 auf, das untere Auflageträger 4 für einen pastöses Gut enthaltenden Behälter 5 aufweist. Oberhalb dieses zylindrischen Behälters 5 ist eine Druckplatte 6 angeordnet, die von einem hydraulisch beaufschlagbaren Arbeitszylinder 7 in den Behälter 5 einpreßbar ist. Dieser Arbeitszylinder 7 stützt sich an einem oberen Querhaupt 8 des Gestells 3 ab. Durch entsprechendes Nachuntendrücken der Druckplatte 6 in den Behälter 5 hinein wird das pastöse Gut aus diesem heraus in eine Transportleitung 9 gedrückt, durch die es einem der Maschine 2 zugeordneten Dosiergerät 10 zugeführt wird.
- Von diesem Dosiergerät 10 wird das pastöse Gut portionsweise in jeweils genau dosierter Menge einer weiter unten noch genauer zu beschreibenden Abfüllstation 11 zugeführt.
- Die Kartuschen-Füll- und Verschließ-Maschine 2 weist im wesentlichen ein langgestrecktes Maschinengestell 12 auf, an dessen einer - in Fig. 1 und 2 jeweils linken-Seite ein Kartuschen-Magazin 13 angebracht ist.
- Der schrittweise Transport von Kartuschen 14 vom Magazin 13 über verschiedene Arbeitsstationen erfolgt mittels eines sogenannten Rechens 15. Hierbei handelt es sich um einen im Maschinengestell 12 gelagerten Schlitten 16, der mittels eines pneumatisch beaufschlagbaren Kolben-Zylinder-Antriebs 17 in Arbeitsrichtung 18 und entgegen dieser Arbeitsrichtung bewegbar ist, und zwar jeweils um das Maß s eines Arbeitsschrittes. An diesem Schlitten 16 sind in vertikaler Richtung, also senkrecht zur Arbeitsrichtung 18, betätigbare pneumatisch beaufschlagbare Kolben-Zylinder-Antriebe 19 angebracht, deren Kolbenstangen 2o eine Transportplatte 21 mit jeweils vier paarweise angeordneten Mitnehmern 22 aufweist, wobei der Abstand jedes Paares von Mitnehmern 22 vom benachbarten Paar gleich dem Maß s eines Arbeitsschrittes ist. Auf dem Maschinengestell 12 selber sind prismatische Auflagen 23 für die Kartuschen 14 vorgesehen, zwischen denen die Transportplatte 21 mit den Mitnehmern 22 des Rechens 15 angeordnet ist. In jedem Paar von Auflagen 23 liegt während des Betriebes eine Kartusche 14. In dieser Stellung befindet sich die Transportplatte 21 etwas unterhalb der Auflagen 23. Zum Weitertransport in Arbeitsrichtung 18 um das Maß s eines Arbeitsschrittes werden zuerst die Antriebe 19 in vertikaler Richtung beaufschlagt, so daß die Kartuschen 14 aus den Auflagen 23 nach oben herausgehoben werden. Anschließend wird der Antrieb 17 derartig beaufschlagt, daß er den gesamten Schlitten l6 mit Rechen 15 in Arbeitsrichtung 18 um das Maß s verfährt. Anschließend werden die Antriebe 19 so beaufschlagt, daß die Transportplatte 21 mit den Mitnehmern 22, also der Rechen 15, nach unten abgesenkt wird, so daß sämtliche Kartuschen 14 wieder in Auflagen 23 abgelegt werden. Der Rechen 15 wird hierbei so weit abgesenkt, daß die Mitnehmer 22 frei zur Unterseite der in den Auflagen 23 liegenden Kartuschen 14 sind. Durch umgekehrte Beaufschlagung des Antriebes 17 wird dann der Rechen wieder in seine Ausgangslage zurückgefahren. Durch dieses Verfahren des Rechens 15 auf einer - von der Seite gesehen-etwa rechteckigen Bahn können die Kartuschen immer um einen Arbeitsschritt in Arbeitsrichtung 18 weitertransportiert werden. Bei den erwähnten Arbeitsstationen handelt es sich außer um die bereits erwähnte Abfüllstation 11 um eine Verschließstation 24 und wahlweise um eine Prägestation 25, in der auf den Kartuschen 14 eine Einprägung angebracht wird. Die verschlossenen Kartuschen 14 verlassen die Maschine 2 an dem dem Magazin 13 entgegengesetzten Ende über eine Abführrampe 26. Der Verschließstation 24 ist eine Sortiervorrichtung 27 für Kolben zum Verschließen der Kartuschen 14 vorgeordnet.
- Die Abfüllstation 11 weist ein in seiner Außenform rohrförmiges Abfüllventil 28 auf, dessen Mittel-Längsachse 29 parallel zu den Mittel-Längs-Achsen 3o der auf den Auflagen 23 liegenden Kartuschen 14 verläuft. Der Außendurchmesser D des Abfüllventils 28 ist etwas kleiner als der Innendurchmesser d der Kartuschen 14, so daß diese vollständig über das Abfüllventil 28 zum Füllen mit pastösem Gut geschoben werden können. Insoweit als die Anlage bis hierher beschrieben ist, ist sie bekannt und verbreitet. Wie insbesondere Fig. 5 entnehmbar ist, ist das Maschinengestell 12 an seiner Oberseite mittels zweier Abdeckplatten 31, 32 abgedeckt, die an ihren einander zugewandten Rändern die Auflagen 23 tragen und zwischen denen der Rechen 15 angeordnet ist. Beiden der Abfüllstation 11 zugehörigen Auflagen 23 sind jeweils eine Abhebeeinrichtung 33 zugeordnet, die einen als Kolben-Zylinder-Antrieb ausgebildeten Abhebeantrieb 34 aufweisen, dessen Zylinder 35 jeweils an der Unterseite der Abdeckplatte 31 bzw. 32 angebracht ist. An der jeweiligen Kolbenstange 36 ist jeweils eine Aufnahme 37 angebracht, mittels derer die entsprechende Kartusche 14 von unten umgriffen werden kann. Durch entsprechende pneumatische Beaufschlagung der Abhebeantriebe 34 kann somit die in den zugehörigen Auflagen 23 befindliche Kartusche 14 aus diesen Auflagen 23 herausgehoben und nach oben zu einer darüber befindlichen Halte-und Zentrier-Vorrichtung 38 für die Kartusche transportiert werden. In dieser oberen Stellung ist die Kartusche 14 in Fig. 5 strichpunktiert dargestellt.
- Diese Halte- und Zentrier-Vorrichtung 38 weist eine zylinderabschnittsförmige der Kartuschenform angepaßte Anlage 39 auf, in der die zylindrische, dünnwandige und leicht verformbare Kartusche 14 so zentriert wird, daß ihre Achse 3o mit der Achse 29 des Abfüllventils 28 fluchtet. Das dem Abfüllventil 28 entgegengesetzte, bereits verschlossene Ende der Kartusche 14 liegt gegen einen als Verschiebesicherung 4o dienenden Anschlag an. Die Kartusche 14 wird in der Anlage 39 mittels zweier Vakuum-Saug-Halter 41 gehalten, von denen nur einer - in Fig. 5 links - dargestellt ist. Diese Vakuum-Saug-Halter 41 weisen jeweils einen faltenbalgartigen Saugschlauch 42 auf, dessen unteres offenes Ende 43 über zylinderabschnittsförmige Anlageflächen 43 der Anlage 39 vorsteht. Durch dieses offene Ende 43 wird über eine nur angedeutete Vakuumleitung 45 Luft angesaugt. Wenn beim bereits geschilderten Anheben der Kartusche 14 mittels der Abhebeeinrichtung 33 die Oberseite der Kartusche gegen die beiden offenen Enden 43 der faltenbalgartigen Saugschläuche 42 kommt, dann werden diese offenen Enden 43 durch die Kartusche 14 verschlossen. Hierdurch bedingt ziehen sich die beiden Saugschläuche 42 aufgrund des in ihnen herrschenden Unterdrucks zusammen, wodurch die Kartusche in die Anlage 39 gezogen und dort gegen die Anlagefläche 44 zentriert und gehalten wird. Diese elastischen faltenbalgartigen Saugschläuche 42 können hierzu auch quer zu ihrer Längsrichtung sich bewegen, so daß ein einwandfreies Zentrieren der Kartusche in der Anlage 39 gewährleistet ist. In der Anlage 39 ist ein Schwenkhebel 46 angeordnet, der von der Kartusche 14, wenn sie in die Anlage 39 hineingezogen wird, angehoben wird. In der zentrierten Lage der Kartusche 14 in der Anlage 39 ist der Schwenkhebel ganz nach oben verschwenkt und betätigt hierdurch einen Signalgeber 47, der eine Folgesteuerung auslöst.
- Die Halte- und Zentrier-Vorrichtung 38 ist an einem rohrförmigen Schlitten 48 angebracht, der auf einer Führungsstange 49 parallel zu den Mittel-Längs-Achsen 29, 3o verschiebbar angeordnet ist. Die Führungsstange 49 ist am Rahmen 5o der Abfüllstation 11 fest angebracht, der wiederum auf dem Maschinengestell 12 angebracht ist. Zum Antrieb des Schlittens 48 und damit der Halte- und Zentrier-Vorrichtung 38 ist ein als pneumatisch beaufschlagbarer Kolben-Zylinder-Antrieb ausgebildeter Verschiebeantrieb 51 vorgesehen, dessen Zylinder 52 am Rahmen 5o befestigt ist, während dessen Kolbenstange 53 mit dem Schlitten 48 verbunden ist. Wenn durch Hochschwenken des Schwenkhebels 46 der Signalgeber 47 - wie erwähnt - ein Signal abgibt, dann wird der Zylinder 52 des Verschiebeantriebs 51 in der Weise mit Druckluft beaufschlagt, daß die Kolbenstange 53 in diesen hineingezogen wird, wodurch der Schlitten 48 mit der Halte- und Zentrier-Vorrichtung 38 derart - in Fig. 4 und 5 nach links - verfahren wird, daß die in der Vorrichtung 38 befindliche Kartusche 14 über das Abfüllventil 28 geschoben wird. Anschließend wird der Zylinder 52 druckentlastet. Gleichzeitig beginnt das Füllen der Kartusche 14, indem vom Dosiergerät 10 eine entsprechende Menge an pastösem Gut durch das Abfüllventil 28 in die Kartusche gedrückt wird. Durch diesen Fülldruck wird die Kartusche 14 entsprechend dem Grad ihrer Füllung von dem Abfüllventil 28 heruntergeschoben, d.h. die Halte- und Zentriervorrichtung 38 wird zusammen mit dem Schlitten 48 wieder in entgegengesetzter Richtung verschoben, wodurch die Kolbenstange 53 aus dem Zylinder 52 des Verschiebeantriebs 51 herausgezogen wird. Am Ende des Füllvorganges wird der Zylinder 52 noch in Ausschubrichtung der Kolbenstange 53 mit Druckluft beaufschlagt, so daß der Schlitten 48 mit der Vorrichtung 38 und der gefüllten Kartusche 14 wieder in die Ausgangsstellung zurückgebracht wird, in der die Kartusche 14 frei vom Abfüllventil 28 ist. Im Anschluß daran wird die Kartusche durch Belüftung der Saugschläuche 42 der Vakuum-Saug-Halter 41 in die Auflagen 23 abgesenkt. Die Abhebeantriebe 34 werden so beaufschlagt, daß die Kartusche 14 abgesenkt und wieder in den Auflagen 23 abgelegt wird. Anschließend wird die Kartusche mittels des Rechens 15 in der bereits geschilderten Weise um einen Arbeitsschritt weitertransportiert, so daß sie in die Verschließstation 24 kommt.
- Die geschilderten Steuervorgänge werden zum einen von einem am Maschinengestell 12 angebrachten Steuerpult 54 und zum anderen von einer zentralen Steuereinrichtung 55 gesteuert.
Claims (6)
- Abfüllstation (11) für eine Kartuschen-Füll- und Verschließ-Maschine (2) zum Abfüllen von zähflüssigem oder pastösem Material in zylindrische Kartuschen (14) mit einem Abfüllventil (28), mit einer Halte- und Zentrier-Vorrichtung (38), die eine Anlage (39) mit einer Anlagefläche (44) zum Halten und Zentrieren der Kartuschen (14) in einer zum Abfüllventil (28) fluchtenden Lage aufweist, und mit einem Verschiebeantrieb (51) zum Verschieben der Halte- und Zentrier-Vorrichtung (38) und des Abfüllventils (28) relativ zueinander, dadurch gekennzeichnet, daß die Halte- und Zentrier-Vorrichtung (38) mindestens einen in der Anlage (39) angeordneten Vakuum-Saug-Halter (41) aufweist, der durch einen faltenbalgartig ausgebildeten Saugschlauch (42) gebildet ist, dessen offenes Ende (43) sich in der Anlage (39) befindet und sich über die Anlagefläche (44) hinaus erstreckt.
- Abfüllstation nach Anspruch 1, dadurch gekennzeichnet, daß die Anlagefläche (44) der Außenform der Kartuschen (14) angepaßt ist.
- Abfüllstation nach Anspruch 2, dadurch gekennzeichnet, daß die Kartusche (14) zylindrisch und die Anlagefläche (44) zylinderabschnittsförmig ausgebildet ist.
- Abfüllstation nach Anspruch 3, dadurch gekennzeichnet, daß die Halte- und Zentrier-Vorrichtung (38) an einem Schlitten (48) angebracht ist, der parallel zur Mittel-Längs-Achse (29, 30) des Abfüllventils (28) und einer in der Halte- und Zentrier-Vorrichtung (38) gehaltenen Kartusche (14) verschiebbar ist.
- Abfüllstation nach Anspruch 1, wobei die Kartuschen (14) in im wesentlichen horizontaler Lage ihrer Mittel-Längs-Achsen (30) durch die Abfüllstation (11) transportierbar sind und wobei Auflagen (23) zur Aufnahme der Kartuschen (14) in einer Ruhelage vorgesehen sind, dadurch gekennzeichnet, daß die Halte- und Zentrier-Vorrichtung (38) oberhalb der Auflagen (23) für eine Kartusche (14) angeordnet ist, daß die Anlage-fläche (44) zur Auflage (23) hin offen ist und daß eine Abhebeeinrichtung (33) zum Abheben der Kartuschen (14) von den Auflagen (23) zur Halte- und Zentrier-Vorrichtung (38) vorgesehen ist.
- Abfüllstation nach Anspruch 5, dadurch gekennzeichnet, daß die Abhebeeinrichtung (33) mindestens einen Abhebeantrieb (34) mit einer Aufnahme (37) für die Kartusche (14) aufweist.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT88104073T ATE76614T1 (de) | 1987-05-14 | 1988-03-15 | Abfuellstation fuer eine kartuschen-fuell- und verschliess-maschine. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3716119 | 1987-05-14 | ||
| DE19873716119 DE3716119A1 (de) | 1987-05-14 | 1987-05-14 | Abfuellstation fuer eine kartuschen-fuell- und verschliess-maschine |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0290747A2 EP0290747A2 (de) | 1988-11-17 |
| EP0290747A3 EP0290747A3 (en) | 1989-10-25 |
| EP0290747B1 true EP0290747B1 (de) | 1992-05-27 |
Family
ID=6327534
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP88104073A Expired - Lifetime EP0290747B1 (de) | 1987-05-14 | 1988-03-15 | Abfüllstation für eine Kartuschen-Füll- und Verschliess-Maschine |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US4874022A (de) |
| EP (1) | EP0290747B1 (de) |
| JP (1) | JPS63307001A (de) |
| AT (1) | ATE76614T1 (de) |
| DE (2) | DE3716119A1 (de) |
| ES (1) | ES2031170T3 (de) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0685396A1 (de) | 1994-06-03 | 1995-12-06 | Ludwig Schwerdtel GmbH. | Fördervorrichtung zum taktweisen Transport von Behältern |
| EP0711982A2 (de) | 1994-11-11 | 1996-05-15 | Ludwig Schwerdtel GmbH. | Dosier-Gerät für viskose Materialien |
| DE102011005741B3 (de) * | 2011-03-17 | 2012-01-26 | Ludwig Schwerdtel Gmbh | Fülleinrichtung zum Abfüllen von hochviskosem Material in zylindrische Kartuschen |
| DE202012005857U1 (de) | 2012-06-14 | 2012-07-12 | Ludwig Schwerdtel Gmbh | Fülleinrichtung zur dosierten Abgabe von hochviskosem Material |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US7793802B2 (en) * | 2006-09-15 | 2010-09-14 | Momentive Performance Materials | Fastener for a viscous material container evacuator and method |
| US20080067192A1 (en) * | 2006-09-15 | 2008-03-20 | Stanton Jennifer L | Viscous material feed system and method |
| US7784503B2 (en) * | 2006-09-29 | 2010-08-31 | Momentive Performance Materials | Viscous material metering system and method |
| US7610167B2 (en) * | 2006-11-08 | 2009-10-27 | Momentive Performance Materials | Controlled material processing device, controller and method |
| US7600658B2 (en) * | 2006-11-28 | 2009-10-13 | Momentive Performance Materials | Viscous material feed system with platen and method |
| CN102390555A (zh) * | 2011-07-06 | 2012-03-28 | 蚌埠市周氏蜂业有限责任公司 | 一种蜂花粉灌装机 |
| US9746129B2 (en) | 2012-09-28 | 2017-08-29 | Momentive Performance Materials Inc. | Puck wear detection |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2839094A (en) * | 1956-10-15 | 1958-06-17 | Horix Mfg Company | Valve for liquid filling apparatus |
| US3115906A (en) * | 1960-05-13 | 1963-12-31 | Continental Oil Co | Grease dispensing apparatus |
| US3227481A (en) * | 1963-02-07 | 1966-01-04 | Vacuum Concrete Corp Of Americ | Vacuum lifter |
| US3237662A (en) * | 1963-03-11 | 1966-03-01 | Richard A Hawley | Stuffing horn for food mold filling machines |
| BE727756A (de) * | 1968-04-29 | 1969-07-01 | ||
| US3656794A (en) * | 1971-01-21 | 1972-04-18 | Diamond Int Corp | Vacuum cup lifter for shell eggs |
| JPS5143422B2 (de) * | 1972-04-18 | 1976-11-22 | ||
| US3788035A (en) * | 1972-06-21 | 1974-01-29 | Container Corp | Caulking cartridge filling and seaming machine |
| FR2398668A1 (fr) * | 1977-07-28 | 1979-02-23 | Chirana Koncern | Dispositif distributeur et doseur de produits tubulaires, notamment de produits medicinaux |
| FR2427976B1 (fr) * | 1978-06-06 | 1985-10-25 | Karlsruhe Augsburg Iweka | Dispositif pour le transfert de recipients de conditionnement |
| DE3116458A1 (de) * | 1981-04-25 | 1982-11-11 | Raku Kunststoff-Verpackungswerke Gmbh, 7550 Rastatt | Verfahren und vorrichtung zum fuellen von behaeltern aus verformbarem material |
| US4712665A (en) * | 1986-08-07 | 1987-12-15 | Ex-Cell-O Corporation | Container lift mechanism |
-
1987
- 1987-05-14 DE DE19873716119 patent/DE3716119A1/de not_active Withdrawn
-
1988
- 1988-03-15 ES ES198888104073T patent/ES2031170T3/es not_active Expired - Lifetime
- 1988-03-15 DE DE8888104073T patent/DE3871436D1/de not_active Expired - Fee Related
- 1988-03-15 EP EP88104073A patent/EP0290747B1/de not_active Expired - Lifetime
- 1988-03-15 AT AT88104073T patent/ATE76614T1/de not_active IP Right Cessation
- 1988-05-05 US US07/195,781 patent/US4874022A/en not_active Expired - Fee Related
- 1988-05-13 JP JP63114990A patent/JPS63307001A/ja active Pending
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0685396A1 (de) | 1994-06-03 | 1995-12-06 | Ludwig Schwerdtel GmbH. | Fördervorrichtung zum taktweisen Transport von Behältern |
| DE4419498A1 (de) * | 1994-06-03 | 1995-12-07 | Schwerdtel Ludwig Gmbh | Fördervorrichtung zum taktweisen Transport von Behältern |
| EP0711982A2 (de) | 1994-11-11 | 1996-05-15 | Ludwig Schwerdtel GmbH. | Dosier-Gerät für viskose Materialien |
| DE102011005741B3 (de) * | 2011-03-17 | 2012-01-26 | Ludwig Schwerdtel Gmbh | Fülleinrichtung zum Abfüllen von hochviskosem Material in zylindrische Kartuschen |
| DE202012005857U1 (de) | 2012-06-14 | 2012-07-12 | Ludwig Schwerdtel Gmbh | Fülleinrichtung zur dosierten Abgabe von hochviskosem Material |
Also Published As
| Publication number | Publication date |
|---|---|
| US4874022A (en) | 1989-10-17 |
| JPS63307001A (ja) | 1988-12-14 |
| ES2031170T3 (es) | 1992-12-01 |
| DE3871436D1 (de) | 1992-07-02 |
| DE3716119A1 (de) | 1988-11-24 |
| ATE76614T1 (de) | 1992-06-15 |
| EP0290747A2 (de) | 1988-11-17 |
| EP0290747A3 (en) | 1989-10-25 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0290747A2 (de) | Abfüllstation für eine Kartuschen-Füll- und Verschliess-Maschine | |
| EP0685396A1 (de) | Fördervorrichtung zum taktweisen Transport von Behältern | |
| DE2334565A1 (de) | Vorrichtung fuer die automatische endbearbeitung und gruppierung von verpackungsbehaeltern | |
| DE4211089C2 (de) | Vorrichtung zur Vereinzelung von gestapelten Ventilsäcken und zum Aufstecken der Ventilsäcke auf den oder die Füllstutzen einer Ventilsackfüllmaschine | |
| DE8717649U1 (de) | Handhabungseinrichtung zum Wechseln der Werkzeuge einer Stanzpresse | |
| EP1520809B1 (de) | Fördervorrichtung und Verfahren zur Anpassung an unterschiedliche Behälterformate | |
| DE2452420C2 (de) | Vorrichtung zum Aufbringen eines Trägers auf Behälter | |
| DE3931710C2 (de) | Non-Stop-Bogenanleger für Bogenrotationsmaschinen | |
| DE3141075C2 (de) | Zuführeinrichtung für Blechstreifenstapel zur Zufuhr zu einem Stanzautomaten | |
| DE1817237B2 (de) | Vorrichtung zum einsetzen von verschluessen in die einfuelloeffnung an der stirnseite von faessern oder dergleichen | |
| DE19932519C5 (de) | Vorrichtung zum Entleeren von Spraydosen | |
| DE2719957C3 (de) | Etikettiervorrichtung | |
| DE19825106C1 (de) | Vorrichtung zum Markieren von Verschlußklammern | |
| EP0312918B1 (de) | Verfahren und Einrichtung zur Herstellung von einen unrunden Querschnitt aufweisenden Dosenkörpern | |
| DE3317084C2 (de) | ||
| DE2443376C2 (de) | Pneumatisch oder hydraulisch betätigbare Rahmenpresse | |
| DE3431974C2 (de) | ||
| EP0266625A2 (de) | Oberer Werkzeugträger für eine Stanze od. dgl. | |
| EP0226008B1 (de) | Magazin zum Stapeln von Blechteilen, insbesondere für die Herstellung von Dosen | |
| DE3335122A1 (de) | Vorrichtung zum handhaben von lagern | |
| DE2012976B2 (de) | Kniehebelprägepresse | |
| EP0111101A1 (de) | Vorrichtung zum Befüllen von Säcken | |
| DE1266230B (de) | Vorrichtung zum einzelweisen Abheben von Scheiben, insbesondere Glasscheiben, von einem in etwa hochkant stehenden Stapel | |
| EP0252167A1 (de) | Maschine zum Ansetzen von Knöpfen, Nieten oder dergleichen an Kleidungsstücke | |
| DE2739279C2 (de) | Vorrichtung zum Pressen von Pulver zu kugelförmigen Preßkörpern |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH DE ES FR GB IT LI NL |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH DE ES FR GB IT LI NL |
|
| 17P | Request for examination filed |
Effective date: 19900405 |
|
| 17Q | First examination report despatched |
Effective date: 19910306 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE ES FR GB IT LI NL |
|
| REF | Corresponds to: |
Ref document number: 76614 Country of ref document: AT Date of ref document: 19920615 Kind code of ref document: T |
|
| ET | Fr: translation filed | ||
| ITF | It: translation for a ep patent filed | ||
| REF | Corresponds to: |
Ref document number: 3871436 Country of ref document: DE Date of ref document: 19920702 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2031170 Country of ref document: ES Kind code of ref document: T3 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 19930209 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19930315 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19930316 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19930331 Ref country code: CH Effective date: 19930331 Ref country code: BE Effective date: 19930331 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| BERE | Be: lapsed |
Owner name: LUDWIG SCHWERDTEL G.M.B.H. Effective date: 19930331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19931001 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19930315 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Effective date: 19940315 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19950215 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19950524 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19961129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19961203 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 19990405 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050315 |