EP2783794B1 - Schleifscheibe sowie Verfahren zu ihrer Verstärkung - Google Patents
Schleifscheibe sowie Verfahren zu ihrer Verstärkung Download PDFInfo
- Publication number
- EP2783794B1 EP2783794B1 EP13161044.6A EP13161044A EP2783794B1 EP 2783794 B1 EP2783794 B1 EP 2783794B1 EP 13161044 A EP13161044 A EP 13161044A EP 2783794 B1 EP2783794 B1 EP 2783794B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- grinding wheel
- bore
- potting compound
- plastic
- poured
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D3/00—Physical features of abrasive bodies, or sheets, e.g. abrasive surfaces of special nature; Abrasive bodies or sheets characterised by their constituents
- B24D3/34—Physical features of abrasive bodies, or sheets, e.g. abrasive surfaces of special nature; Abrasive bodies or sheets characterised by their constituents characterised by additives enhancing special physical properties, e.g. wear resistance, electric conductivity, self-cleaning properties
- B24D3/348—Physical features of abrasive bodies, or sheets, e.g. abrasive surfaces of special nature; Abrasive bodies or sheets characterised by their constituents characterised by additives enhancing special physical properties, e.g. wear resistance, electric conductivity, self-cleaning properties utilised as impregnating agent for porous abrasive bodies
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D18/00—Manufacture of grinding tools or other grinding devices, e.g. wheels, not otherwise provided for
- B24D18/0027—Manufacture of grinding tools or other grinding devices, e.g. wheels, not otherwise provided for by impregnation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D5/00—Bonded abrasive wheels, or wheels with inserted abrasive blocks, designed for acting only by their periphery; Bushings or mountings therefor
- B24D5/02—Wheels in one piece
- B24D5/04—Wheels in one piece with reinforcing means
Definitions
- the invention relates to a method for reinforcing a grinding wheel according to the preamble of claim 1.
- Such grinding wheels are used, for example, in the machining of gears for car transmissions.
- it is endeavored to steadily increase the cutting speeds in continuous generating grinding.
- safety standards must be adhered to, according to which the permissible cutting speed must be in a specific relationship to the blasting speed of the grinding wheel.
- a disadvantage of this device is the relatively complicated structure and the risk of breakage of the abrasive body during the tensioning of the same between these flanges.
- the risk that this is not uniform, but in the lower part by gravity creates a higher density.
- synthetic resins also uneconomical epoxy resins are used because of the high cost.
- the publication DE-A-1 261 772 refers to a method for making a reinforcing hub inside a grinding wheel by centrifugal casting, in which this reinforcing hub merges homogeneously into the grinding wheel.
- the invention is the object of the invention to provide a method for reinforcing a grinding wheel of the type mentioned that an increase in the blasting speed during operation of the grinding wheel is made possible.
- the grinding wheel according to the invention with preferably horizontally oriented axis of rotation is rotated and cast, for example, 400 rpm (revolutions per minute) a certain amount potting compound in the hole, wherein by adjusting the spin speed and / or the amount of liquid and the Curing time of the potting compound used, the penetration depth of the adhesive into the grinding wheel and the thickness of the reinforcing ring can be set within certain limits.
- the invention provides to attach the grinding wheel on the outside sealing elements, which should prevent that the cast-in casting compound runs out laterally uncontrolled.
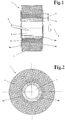
- the arrangement according to Fig. 1 shows a grinding wheel 1 of porous ceramic material, wherein it is preferably made of corundum. Of course, instead of corundum other similarly porous structured ceramic materials may be considered.
- the grinding wheel 1 is provided with a bore 2 in particular for its attachment to a spindle of a machine tool. According to the invention, at least one cast-in plastic material forms both a ring 2a lining the bore 2 and this reinforcing layer 2b in the grinding wheel pores 1 '.
- the grinding wheel is made of an open to highly porous structure, advantageously with a porosity of over 50 percent by volume.
- a potting compound is used from a 2-component polyurethane system, which is particularly suitable both in terms of its physical properties and because of its economy potting compound for producing the ring 2a and for filling the disc pores 1 'in Area of the annular reinforcing layer 2b.
- Other suitable casting compounds can be used.
- the pouring of the potting compound into the bore 2 of the grinding wheel 1 is effected by means of a casting device, of which only just a feed nozzle 5 is shown, which directs the potting compound in the region of the bore 2.
- a casting device of which only just a feed nozzle 5 is shown, which directs the potting compound in the region of the bore 2.
- In order to prevent uncontrolled leakage of the potting compound after the supply line in the bore 2 are on the grinding wheel 1 arranged on the outside sealing elements 8a, 8b provided.
- the grinding wheel 1 For producing the ring 2 a surrounding the bore 2 as well as the reinforcing layer 2 b in the grinding wheel pores 1 'of the grinding wheel 1, this is rotated by a drive, not shown, about the horizontally oriented axis of rotation 6, while through the casting device with the supply nozzle 5 a certain amount Potting compound is supplied.
- the grinding wheel 1 rotates at a speed of, for example, 400 rpm (revolutions per minute), wherein the cast-in casting compound penetrates into the pores 1 'of the grinding wheel 1 through the then acting centrifugal force and bonds with its ceramic material.
- the achievable penetration depth 4 and also the wall thickness 3 of the ring 2a are dependent on the spin speed and the cast amount, as well as the degree of liquid and the curing time of the potting compound used. By varying these sizes, the wall thickness 3 or penetration depth of the potting compound and the thickness of the reinforcing layer 2b can be regulated within certain limits.
- the cast-in plastic for forming the ring as well as the reinforcing layer in the grinding wheel pores could be formed by a layered casting with different materials of potting or adhesive masses.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Polishing Bodies And Polishing Tools (AREA)
- Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)
Description
- Die Erfindung betrifft ein Verfahren zum Verstärken einer Schleifscheibe nach dem Oberbegriff des Anspruchs 1.
- Derartige Schleifscheiben kommen beispielsweise bei der Bearbeitung von Zahnrädern für Autogetriebe zum Einsatz. Um die Produktivität und die Wirtschaftlichkeit des Schleifprozesses zu verbessern, ist man bestrebt, die Schnittgeschwindigkeiten beim kontinuierlichen Wälzschleifen stetig zu erhöhen. Dabei sind Sicherheitsnormen einzuhalten, nach welchen die zulässige Schnittgeschwindigkeit in einem bestimmten Verhältnis zur Sprenggeschwindigkeit der Schleifscheibe stehen muss.
- Die Verstärkung der Schleifscheibe im Bereich der Bohrung ermöglicht zwar höhere zulässige Schnittgeschwindigkeiten, bringt aber einen ebenfalls höheren Fertigungsaufwand mit sich. Das gilt auch bei einer bekannten Schleifscheibe gemäss der Druckschrift
JP-A-2000153 464 - In der Druckschrift
AT-502 845
Nachteilig bei dieser Vorrichtung ist der relativ komplizierte Aufbau und der Gefahr eines Brechens des Schleifkörpers bei der Verspannung desselben zwischen diesen Flanschen. Zudem besteht bei diesem Einfüllen bei vertikaler Achse in den Spalt die Gefahr, dass diese nicht gleichmässig erfolgt, sondern im unteren Bereich durch die Schwerkraft eine höhere Dichte entsteht. Als Kunstharze sind ausserdem wegen den hohen Kosten unwirtschaftliche Epoxidharze verwendet.
Die DruckschriftDE-A-1 261 772 bezieht sich auf ein Verfahren zur Herstellung einer Verstärkungsnabe im Innern einer Schleifscheibe mittels Schleuderguss, bei der diese Verstärkungsnabe homogen in die Schleifscheibe übergeht. Nachteilig hierbei ist, dass eine solche Herstellung von Verstärkungsnaben ohne eine entsprechende Vorrichtung dazu führt, dass das Kunstharz seitlich bei der Schleifscheibe nicht eben erzeugt werden kann und durch Nachbearbeitung geschliffen werden muss. Es wird ebenfalls als Kunstharz ein teures Epoxidharz verwendet. - Der Erfindung liegt demgegenüber die Aufgabe zugrunde, ein Verfahren zum Verstärken einer Schleifscheibe der eingangs genannten Art zu schaffen, dass eine Steigerung der Sprenggeschwindigkeit im Betrieb der Schleifscheibe ermöglicht wird.
- Diese Aufgabe ist erfindungsgemäss durch die Merkmale des Anspruchs 1 bzw. des Anspruchs 4 gelöst.
- Durch die Verstärkung der Schleifscheibe mit einer geeigneten Vergussmasse wird eine innige Verbindung zwischen ihm und dem porösen Material der Schleifscheibe hergestellt, weil diese bis in die feinsten Scheibenporen einfliessende Vergussmasse ein festes Gefüge mit dem Material der Schleifscheibe sicherstellt. Die Vergussmasse in die Bohrung der rotierenden Schleifscheibe einzugiessen und dabei die Eindringtiefe des Verstärkungsmaterials zu regulieren, ist herstellungstechnisch einfach zu realisieren. Auf diese Weise lässt sich auch die Stärke des die Bohrung auskleidenden Verstärkungsrings innerhalb bestimmter Grenzwerte variieren.
- Zur Herstellung der Verstärkung wird die Schleifscheibe erfindungsgemäss mit vorzugsweise horizontal ausgerichteter Rotationsachse in Drehung versetzt und von beispielsweise 400 rpm (Umdrehungen pro Minute) eine bestimmte Menge Vergussmasse in die Bohrung eingegossen, wobei durch Anpassung der Schleuderdrehzahl und/oder der Menge, des Flüssigkeitsgrades und der Aushärtezeit der verwendeten Vergussmasse die Eindringtiefe des Klebstoffs in die Schleifscheibe und die Stärke des Verstärkungsrings innerhalb bestimmter Grenzwerte einstellbar ist. Die Erfindung sieht vor, der Schleifscheibe aussenseitig Dichtungselemente anzubringen, die verhindern sollen, das die eingegossene Vergussmasse seitlich unkontrolliert herausläuft.
- Die Erfindung ist nachfolgend anhand eines Ausführungsbeispiels unter Bezugnahme auf die Zeichnung näher erläutert. Es zeigt:
- Fig. 1
- eine Anordnung zum Verstärken einer Schleifscheibe mit einer Vergussmasse, im Schnitt und schematisch dargestellt, und
- Fig. 2
- eine Seitenansicht der Schleifscheibe.
- Die Anordnung gemäss
Fig. 1 zeigt eine Schleifscheibe 1 aus porösem keramischen Material, wobei sie vorzugsweise aus Korund hergestellt ist. Anstelle von Korund können selbstverständlich auch andere ähnlich porös strukturierte keramische Materialien in Frage kommen. Die Schleifscheibe 1 ist dabei mit einer Bohrung 2 insbesondere für ihre Befestigung auf einer Spindel einer Werkzeugmaschine versehen.
Erfindungsgemäss ist durch zumindest einen eingegossenen Kunststoff sowohl ein die Bohrung 2 auskleidender Ring 2a als auch diese Verstärkungsschicht 2b in den Schleifscheibenporen 1' gebildet. Die Schleifscheibe ist aus einem offenen bis hochporösen Gefüge hergestellt, vorteilhaft mit einer Porosität von über 50 Volumenprozenten.
Für den zur Verstärkung der Schleifscheibe vorgesehenen Kunststoff wird eine Vergussmasse aus einem 2-Komponenten Polyurethansystem verwendet, der sowohl hinsichtlich seiner physikalischen Eigenschaften als auch wegen seiner Wirtschaftlichkeit besonders geeignet ist für die Verwendung Vergussmasse zur Erzeugung des Ringes 2a und zum Füllen der Scheibenporen 1' im Bereich der ringförmigen Verstärkungsschicht 2b. Selbstverständlich sind auch andere geeignete Vergussmassen verwendbar.
Das Eingiessen der Vergussmasse in die Bohrung 2 der Schleifscheibe 1 erfolgt mittels einer Giesseinrichtung, von welcher nur gerade eine Zufuhrdüse 5 dargestellt ist, welche die Vergussmasse in den Bereich der Bohrung 2 leitet. Um ein unkontrolliertes Auslaufen der Vergussmasse nach der Zuleitung in die Bohrung 2 zu verhindern, sind an der Schleifscheibe 1 aussenseitig angeordnete Dichtungselemente 8a, 8b vorgesehen. - Zur Herstellung des die Bohrung 2 umgebenden Ringes 2a als auch der Verstärkungsschicht 2b in den Schleifscheibenporen 1' der Schleifscheibe 1 wird diese durch einen nicht gezeigten Antrieb um die horizontal ausgerichtete Drehachse 6 in Drehung versetzt, während durch die Giesseinrichtung mit der Zufuhrdüse 5 eine bestimmte Menge Vergussmasse zugeführt wird. Die Schleifscheibe 1 dreht sich dabei mit einer Geschwindigkeit von beispielsweise 400 rpm (Umdrehungen pro Minute), wobei die eingegossene Vergussmasse durch die dann wirkende Schleuderkraft in die Poren 1' der Schleifscheibe 1 eindringt und sich mit ihrem keramischen Material verbindet.
- Die dabei erzielbare Eindringtiefe 4 und genauso die Wandstärke 3 des Ringes 2a sind abhängig von der Schleuderdrehzahl und der eingegossenen Menge, sowie auch vom Flüssigkeitsgrad und der Aushärtezeit der verwendeten Vergussmasse. Durch Variieren dieser Grössen lässt sich die Wandstärke 3 bzw. Eindringtiefe der Vergussmasse und die Stärke der Verstärkungsschicht 2b innerhalb bestimmter Grenzwerte regulieren.
- Um noch höhere Sprenggeschwindigkeiten zu erreichen, ist es grundsätzlich auch möglich, die Schleifscheibe zusätzlich mit einem eingeklebten Metallring zu verstärken, dies allerdings bei Inkaufnahme eines entsprechend höheren apparativen und fertigungstechnischen Aufwands. Ein oder mehrere Metallringe, -drähte oder dergleichen könnten auch beim Eingiessen der Vergussmasse in der Bohrung eingelegt sein und von dem Klebstoff umgossen und nach dem Aushärten in dem Ring 2a eingebettet sein.
- Im Prinzip könnte der eingegossene Kunststoff zur Bildung des Ringes als auch der Verstärkungsschicht in den Schleifscheibenporen durch ein schichtweises Eingiessen mit unterschiedlichen Materialien von Verguss- bzw. Klebstoffmassen gebildet sein.
Claims (5)
- Verfahren zum Verstärken einer Schleifscheibe, vorzugsweise zum Schleifen von Zahnrädern, mit einer für ihre Befestigung dienende Bohrung (2), wobei durch zumindest einen eingegossenen Kunststoff sowohl ein die Bohrung (2) auskleidender Ring (2a) als auch eine Verstärkungsschicht (2b) in den Schleifscheibenporen gebildet sind, wobei an der Aussenseite der Schleifscheibe (1) Dichtungselemente (8a, 8b) zum Verhindern eines unkontrollierten Auslaufens der einzugiessenden Vergussmasse in die Bohrung (2) angebracht sind, dadurch gekennzeichnet, dass
die Schleifscheibe (1) mit horizontal ausgerichteter Rotationsachse (6) in Drehung versetzt und eine bestimmte Menge Vergussmasse als Kunststoff in die Bohrung (2) gegossen wird, welche durch die erzeugte Schleuderkraft in die Poren (1') der Schleifscheibe (1) eindringt und sich mit ihrem keramischen Material verbindet, wobei die Schleifscheibe mit einem offenen bis hochporösen Gefüge hergestellt ist und der eingegossene Kunststoff aus einem Zwei- oder Mehrkomponenten Polyurethansystem besteht. - Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass die Wandstärke (3) des Ringes (2a) und die Eindringtiefe (4) der Vergussmasse durch Verändern der Schleuderdrehzahl, der Menge und Flüssigkeitsgrad der eingegossenen Vergussmasse und/oder der Aushärtezeit der verwendeten Vergussmasse einstellbar ist.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, dass die Schleifscheibe (1) mit einer annähernd konstanten Drehzahl von vorzugsweise 400 rpm (Umdrehungen pro Minute) gedreht wird.
- Schleifscheibe, die nach dem Verfahren nach einem der vorhergehenden Ansprüche 1 bis 3 verstärkt ist, dadurch gekennzeichnet, dass die Schleifscheibe mit einem offenen bis hochporösen Gefüge hergestellt ist und der eingegossene Kunststoff aus einem Zwei- oder Mehrkomponenten Polyurethansystem besteht.
- Schleifscheibe nach Anspruch 4, dadurch gekennzeichnet, dass die Wandstärke (3) des die Bohrung (2) auskleidenden Ringes (2a) bzw. die Eindringtiefe (4) des Kunststoffes in dieser Verstärkungsschicht (2b) einstellbar sind.
Priority Applications (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP13161044.6A EP2783794B1 (de) | 2013-03-26 | 2013-03-26 | Schleifscheibe sowie Verfahren zu ihrer Verstärkung |
| JP2016504521A JP6411453B2 (ja) | 2013-03-26 | 2014-02-05 | 研削砥石及び該研削砥石を補強する方法 |
| CN201480018362.1A CN105263675B (zh) | 2013-03-26 | 2014-02-05 | 磨轮以及用于对其进行强化的方法 |
| KR1020157029941A KR102204558B1 (ko) | 2013-03-26 | 2014-02-05 | 그라인딩 휠 및 이의 보강 방법 |
| US14/779,049 US9839990B2 (en) | 2013-03-26 | 2014-02-05 | Grinding wheel and method of reinforcing the same |
| PCT/EP2014/052211 WO2014154386A1 (de) | 2013-03-26 | 2014-02-05 | Schleifscheibe sowie verfahren zu ihrer verstärkung |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP13161044.6A EP2783794B1 (de) | 2013-03-26 | 2013-03-26 | Schleifscheibe sowie Verfahren zu ihrer Verstärkung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2783794A1 EP2783794A1 (de) | 2014-10-01 |
| EP2783794B1 true EP2783794B1 (de) | 2017-09-27 |
Family
ID=47997131
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP13161044.6A Active EP2783794B1 (de) | 2013-03-26 | 2013-03-26 | Schleifscheibe sowie Verfahren zu ihrer Verstärkung |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US9839990B2 (de) |
| EP (1) | EP2783794B1 (de) |
| JP (1) | JP6411453B2 (de) |
| KR (1) | KR102204558B1 (de) |
| CN (1) | CN105263675B (de) |
| WO (1) | WO2014154386A1 (de) |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CA2959779C (en) | 2016-03-04 | 2019-06-11 | The Libman Company | Scissor-style toilet brush |
| CN107225517B (zh) * | 2017-05-26 | 2019-06-14 | 江苏锋芒复合材料科技集团有限公司 | 一种防漏防水型环保磨砂盘及其制备方法 |
| CH716096B1 (de) * | 2019-09-24 | 2020-11-13 | Reishauer AG | Abrichtwerkzeug sowie ein Verfahren zum Auftragen von Hartstoffpartikeln. |
| CN113967879B (zh) * | 2021-11-04 | 2022-12-27 | 东阳市灿红磁业有限公司 | 一种磨削磨轮和磨削装置 |
| EP4516437B1 (de) | 2023-09-04 | 2025-10-22 | Krebs & Riedel Schleifscheibenfabrik GmbH & Co. KG | Wälzschleifwerkzeug zur hartfeinbearbeitung von verzahnungskomponenten durch kontinuierliches wälzschleifen |
| USD1106288S1 (en) * | 2024-05-31 | 2025-12-16 | Bingtao Fan | Grinding wheel |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH489334A (de) * | 1968-10-11 | 1970-04-30 | Impregnated Diamond Prod Ltd | Diamantschleifwerkzeug und Verfahren zu dessen Herstellung |
| US3526063A (en) * | 1965-03-08 | 1970-09-01 | Norton Co | Integral mounting means and reinforcement for grinding wheels |
Family Cites Families (27)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1884279A (en) * | 1931-08-29 | 1932-10-25 | Hans P Scheel | Pulp grinding stone |
| US2004630A (en) * | 1932-12-06 | 1935-06-11 | Krug Carl | Grinding disk |
| US2006308A (en) * | 1933-07-13 | 1935-06-25 | Norton Co | Grinding wheel |
| US2094556A (en) * | 1935-10-25 | 1937-09-28 | Norton Co | Grinding wheel |
| DE1261772B (de) * | 1955-05-02 | 1968-02-22 | Minnesota Mining & Mfg | Verfahren zur Herstellung einer Verstaerkungsnabe an einer Schleifscheibe mit Kunstharzbindung mittels Schleuderguss |
| ES352979A1 (es) * | 1967-04-28 | 1970-01-16 | Norton Co | Procedimiento para fabricar un dispositivo abrasivo perfe- ccionado. |
| US3939612A (en) * | 1971-06-02 | 1976-02-24 | Dresser Industries, Inc. | Reinforced grinding wheel |
| JPS515113Y2 (de) * | 1971-08-07 | 1976-02-12 | ||
| DE2421260A1 (de) * | 1973-05-14 | 1974-12-05 | Karlstad Mekaniska Ab | Wellenanordnung zum befestigen eines schleifsteins in zellulose-schleifmaschinen |
| JPS5048292U (de) * | 1973-08-28 | 1975-05-13 | ||
| SE401472B (sv) * | 1975-07-23 | 1978-05-16 | Slipmaterial Naxos Ab | Slipskiva bestaende av tva eller flera hopfogade slipelement |
| US4137516A (en) * | 1977-10-31 | 1979-01-30 | Carnegie-Mellon University | Grinding wheel crack detector |
| US5343656A (en) * | 1989-08-01 | 1994-09-06 | Hurth Maschinen Und Werkzeuge G.M.B.H. | Grinding tool and the like made of a ceramic material coated with extremely hard abrasive granules |
| FR2718379B3 (fr) * | 1994-04-12 | 1996-05-24 | Norton Sa | Meules super abrasives. |
| JPH08174430A (ja) * | 1994-12-27 | 1996-07-09 | Tone Corp | 鋳鉄管内面粗研削仕上げ用電着砥石および その取付け構造 |
| JP2000153464A (ja) | 1998-11-16 | 2000-06-06 | Kyowa Rejinasu Kk | 砥石及び砥石の製造方法 |
| JP2001205566A (ja) * | 2000-01-26 | 2001-07-31 | Noritake Co Ltd | 樹脂含浸ビトリファイド砥石およびその製造方法 |
| US6257963B1 (en) | 2000-05-12 | 2001-07-10 | Reishauer Ag | Grinding worm for the continuous generating grinding of gear wheels |
| FR2811599B1 (fr) * | 2000-07-11 | 2003-01-17 | Essilor Int | Procede pour ameliorer la precision d'une operation de chanfreinage appliquee a un verre de lunettes, et outil de chanfreinage correspondant |
| JP2003039331A (ja) * | 2001-08-01 | 2003-02-13 | Noritake Co Ltd | 樹脂製コア部を有する砥石車とその製造方法及び再利用方法 |
| JP2004142029A (ja) * | 2002-10-24 | 2004-05-20 | Noritake Co Ltd | ビトリファイド研削砥石 |
| DE102004013014A1 (de) | 2004-03-16 | 2005-10-06 | Reishauer Ag | Vorrichtung zur Befestigung eines Werkzeugträgers |
| JP2007012810A (ja) * | 2005-06-29 | 2007-01-18 | Renesas Technology Corp | 半導体集積回路装置の製造方法 |
| AT502845B1 (de) * | 2005-11-16 | 2008-04-15 | Rappold Winterthur Technologie | Keramisch gebundene, rotationssymmetrische schleifkörper |
| US8628385B2 (en) * | 2008-12-15 | 2014-01-14 | Saint-Gobain Abrasives, Inc. | Bonded abrasive article and method of use |
| CN202151831U (zh) * | 2011-01-04 | 2012-02-29 | 李海锋 | 一种新型砂轮 |
| ES2756849T3 (es) | 2013-08-07 | 2020-04-27 | Reishauer Ag | Herramienta rectificadora y procedimiento para su fabricación |
-
2013
- 2013-03-26 EP EP13161044.6A patent/EP2783794B1/de active Active
-
2014
- 2014-02-05 JP JP2016504521A patent/JP6411453B2/ja active Active
- 2014-02-05 WO PCT/EP2014/052211 patent/WO2014154386A1/de not_active Ceased
- 2014-02-05 KR KR1020157029941A patent/KR102204558B1/ko active Active
- 2014-02-05 CN CN201480018362.1A patent/CN105263675B/zh active Active
- 2014-02-05 US US14/779,049 patent/US9839990B2/en active Active
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3526063A (en) * | 1965-03-08 | 1970-09-01 | Norton Co | Integral mounting means and reinforcement for grinding wheels |
| CH489334A (de) * | 1968-10-11 | 1970-04-30 | Impregnated Diamond Prod Ltd | Diamantschleifwerkzeug und Verfahren zu dessen Herstellung |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2783794A1 (de) | 2014-10-01 |
| US9839990B2 (en) | 2017-12-12 |
| US20160158919A1 (en) | 2016-06-09 |
| CN105263675A (zh) | 2016-01-20 |
| KR20150133783A (ko) | 2015-11-30 |
| JP6411453B2 (ja) | 2018-10-24 |
| JP2016514623A (ja) | 2016-05-23 |
| WO2014154386A1 (de) | 2014-10-02 |
| KR102204558B1 (ko) | 2021-01-19 |
| CN105263675B (zh) | 2018-04-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2783794A1 (de) | Schleifscheibe sowie Verfahren zu ihrer Verstärkung | |
| EP0095055B1 (de) | Verfahren zur Herstellung eines Schleifkörpers | |
| DE3030914C2 (de) | Verfahren zur Herstellung von Maschinenständern mittels Polymerbeton | |
| DE112015001183T5 (de) | Verfahren zur Herstellung eines Kerns, und Verfahren zur Herstellung eines Turbinenelements unter Verwendung eines mit dem Kernherstellungsverfahren erhaltenen Kerns | |
| DE2334796C2 (de) | Verfahren und Vorrichtung zum Herstellen eines Rohres aus Beton o.dgl. | |
| EP2781772B1 (de) | Gasdrucklagerelement u. Verfahren zur Herstellung eines Gasdrucklagerelements sowie Gasdrucklager mit einem solchen Gasdrucklagerelement | |
| DE102022202959A1 (de) | Rotor für eine Axialflussmaschine, Axialflussmaschine, Kraftfahrzeug und Verfahren zur Befestigung eines Magneten auf einem Flansch eines Rotors | |
| EP3000558B1 (de) | Werkzeug zum bearbeiten von materialien | |
| DE3734328C2 (de) | Beschichtungsverfahren für eine Kunststoff-Schneckenstrangpresse | |
| DE2217824C2 (de) | Verfahren zum Einkapseln von Ständern elektrischer Maschinen in Kunststoff-Einbettungsmassen und Vorrichtung zur Durchführung dieses Verfahrens | |
| DE102012005085A1 (de) | Werkzeug zum Bearbeiten von Materialien | |
| DE1934167A1 (de) | Verfahren und Vorrichtung zur Herstellung von Raedern | |
| EP3219439B1 (de) | Schleifscheibe | |
| EP0799111B1 (de) | Recyclefähige schleifkörperzonen | |
| WO2023233035A1 (de) | Schleifwerkzeug zur bearbeitung von zahnrädern | |
| AT515475B1 (de) | Herstellung einer Topfscheibe | |
| AT502845B1 (de) | Keramisch gebundene, rotationssymmetrische schleifkörper | |
| WO2008058859A1 (de) | Verfahren zur endbearbeitung von konischen stirnradverzahnungen und vorrichtung zur durchführung des verfahrens | |
| WO2012019678A1 (de) | Apparat und verfahren zum vergiessen von hohlfasern | |
| DE10103435C2 (de) | Schleifwerkzeug und Verfahren zu dessen Herstellung | |
| DE9420676U1 (de) | Recyclefähige Schleifkörperzonen | |
| WO2017060108A1 (de) | Reibring mit einer nut für eine scheibenbremse | |
| EP1613867A1 (de) | Walzenbeschichtungsverfahren und beschichtete walze | |
| DE102006012926A1 (de) | Werkzeug zum Bearbeiten von Oberflächen und Verfahren zur Herstellung eines solchen Werkzeugs | |
| DE3740868A1 (de) | Vorrichtung zum auskleiden von bohrloechern |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 17P | Request for examination filed |
Effective date: 20130326 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| R17P | Request for examination filed (corrected) |
Effective date: 20150320 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| 17Q | First examination report despatched |
Effective date: 20150506 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20170517 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 931544 Country of ref document: AT Kind code of ref document: T Effective date: 20171015 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502013008420 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: LUCHS AND PARTNER AG PATENTANWAELTE, CH |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171227 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20170927 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171228 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171227 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180127 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502013008420 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| 26N | No opposition filed |
Effective date: 20180628 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20180326 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20180331 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180326 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180326 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180331 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180326 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20130326 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 Ref country code: MK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170927 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20200324 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210331 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: U11 Free format text: ST27 STATUS EVENT CODE: U-0-0-U10-U11 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260401 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20260320 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20260319 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20260401 Year of fee payment: 14 |