EP1260444B1 - Verpackungsvorrichtung - Google Patents
Verpackungsvorrichtung Download PDFInfo
- Publication number
- EP1260444B1 EP1260444B1 EP02005348A EP02005348A EP1260444B1 EP 1260444 B1 EP1260444 B1 EP 1260444B1 EP 02005348 A EP02005348 A EP 02005348A EP 02005348 A EP02005348 A EP 02005348A EP 1260444 B1 EP1260444 B1 EP 1260444B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- packaging
- folding
- module
- cardboard
- carton
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004806 packaging method and process Methods 0.000 title claims abstract description 46
- 239000005022 packaging material Substances 0.000 claims description 25
- 239000000853 adhesive Substances 0.000 abstract description 10
- 230000001070 adhesive effect Effects 0.000 abstract description 10
- 238000004519 manufacturing process Methods 0.000 description 10
- 239000004831 Hot glue Substances 0.000 description 3
- 238000006243 chemical reaction Methods 0.000 description 2
- 238000013461 design Methods 0.000 description 2
- 239000012943 hotmelt Substances 0.000 description 2
- 238000003754 machining Methods 0.000 description 2
- 238000012858 packaging process Methods 0.000 description 2
- 238000012545 processing Methods 0.000 description 2
- 238000012546 transfer Methods 0.000 description 2
- 238000010276 construction Methods 0.000 description 1
- 238000010924 continuous production Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000011144 upstream manufacturing Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/04—Machines constructed with readily-detachable units or assemblies, e.g. to facilitate maintenance
Definitions
- the present invention relates to a packaging device.
- Packaging devices which have one or more stationarily arranged folding devices, which are essentially equipped with a punch and a die.
- a cut, plate-shaped packaging material blank is inserted into the folding device, provided with an adhesive and folded into a lower carton.
- After removal of the sub-carton is made using the same folding device or a second folding device and using a further packaging material blank in the same way a separate top board (here: lid).
- lid After completion of top and bottom carton is manually or mechanically inserted an object to be packaged in the sub-carton and then closed the sub-carton with the binding therein by attaching the top carton.
- a cut, and for example one-piece, plate-shaped packaging material blank from which both a sub-carton and an integral top carton is foldable is placed with a placed on the blank surface to be packaged article or part on a continuous line and fed to a folding device.
- portions of the packaging material blank are provided with an adhesive;
- portions of the packaging material blank are folded around the article to be packaged, so that a sub-carton is formed, in which the article is already partially packed.
- the sub-carton with the object therein is in the direction of passage to a spatially separated from the folding device or spatially transported spaced locking device.
- further portions of the packaging material blank are provided with an adhesive, and by means of closure elements, an upper carton is folded from the same packaging material blank and sealed over the lower carton, whereby the article is now completely packaged.
- the folding and closing elements are usually designed to be adjustable in size, so that packaging of very different sizes can also be produced without major retooling work. Due to the flow principle and the associated spatially separate arrangement of folding and closing device, however, such devices have a voluminous design and require a very large footprint. Also, extra transport means are to be provided, which transfer the sub-carton or the semi-finished packaging from the folding device to the closure device. As a result of the flow principle and the fixed arrangement of the folding and closing device, the transport device and any further upstream or downstream auxiliary devices, this device concept can not be modified without further modifications or adapted to the respective additional devices.
- EP 0 983 940 A discloses a packaging device according to the preamble of claim 1.
- the invention is based on the object or the technical problem to provide a novel packaging device which avoids the disadvantages of the prior art as far as possible and both a comparatively simple and effective packaging ensures an object as well as more easily adaptable to varying production situations.
- This object is achieved by a packaging device according to the invention with the features of claim 1.
- This packaging device comprises a single, stationarily arranged, modularly expandable packaging center with an integrated, stamp and die-free folding and closing device with size-adjustable folding, closure and adhesive application elements.
- the folding and closing device belong together in the packaging device according to the invention immediately functional.
- the packaging device according to the invention unlike the devices which operate on the continuous-flow principle, all the steps required for the packaging of a respective article, i. applying an adhesive to the packaging material blank, folding the packaging material blank into a sub-carton that may already contain the article to be packaged, and closing the sub-carton by a top carton, preferably folded from the same packaging material blank, in a single unitary stationarily arranged packaging center.
- the packaging device according to the invention is thus not only very compact and space-saving, it also requires no extra transport device to transfer the semi-finished packaging from the folding device to the closure device. Rather, the packaging blank may be processed stationarily at a single processing position and the article packaged at that position. This is advantageous not only when the device according to the invention is operated manually, since for almost all operating activities only a single person in a single location is required, but also when the device, for example, for the purpose of further Automation by additional device components, such as robots, to be extended.
- the packaging device according to the invention similar to the devices operating according to the continuous flow principle, is also equipped with a stamping and die-free folding and closing device with size-adjustable folding, closing and adhesive application elements, but which are all included in the individual packaging center, the packaging device according to the invention is nevertheless the stationary arrangement of the packaging center suitable for the production of packaging of various sizes. Elaborate conversions or the like are not required for this purpose. Even small series are effective and economical to manufacture.
- the article to be packaged can already be arranged on the packaging material blank during the production of its outer packaging, whereby a further rationalization and a high packaging speed are achieved.
- the packaging device according to the invention can also be particularly simple, without great effort and extremely flexible with any other, additional Combine device components and easily adapt to different production situations.
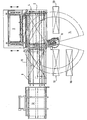
- the figure shows a schematic plan view of a packaging device according to the invention with additional additional device modules.
- the packaging device according to the invention comprises a single, stationarily arranged, modularly expandable, packaging center 2 with an integrated, stamp and die-free folding device 4 and a closure device 6 with size-adjustable folding, closure and adhesive application elements.
- the packaging center 2 forms a kind of individual "packaging cell”.
- the folding device 4 and the closure device 6 are arranged in the present embodiment on a common frame of the packaging center 2.
- the folding elements may be, for example, slides and / or folding flaps, the closure elements may be closure slides and / or counterpressure bars and / or stirrups, and the adhesive application elements may be application nozzles or the like. With the application nozzles, for example, an adhesive in the form of a hot melt adhesive (hot melt adhesive, or similar means) can be applied.
- the packaging device further comprises a packaging material alignment module 10 equipped with a support ramp 8, which is arranged on a left side of the packaging center 2 in the drawing and is coupled or combined in a modular manner with the packaging center 2.
- the alignment module 10 simultaneously functions as a packaging material loading module in the present example.
- a packaging material magazine module 12 is arranged, which is coupled or combined modularly with the alignment module 10 and, in turn, with the packaging center 2.
- a parts loading and unloading module 14 for loading the stationary packaging center 2 with parts to be packed is arranged in the present embodiment, left before the packaging center 2 and combined with this modular.
- the parts loading and unloading module 14 here comprises an industrial robot 16, which removes the parts to be packaged from a parts stack 18, hangs on the packaging material in the region of the alignment module 10 and later removes the finished packaged parts together with their packaging from the packaging center 2 and assembles into a package stack 20.
- the packaging material with which parts or objects are to be packaged is a Fefco 04110 board blank.
- the carton blank will be briefly referred to below as carton.
- the invention is however, of course, not limited to this packaging material and the said standard. In principle, other suitable packaging materials or cardboard can be processed with the device according to the invention.
- the magazine module 12 is filled with a cardboard stack. Then, a cardboard is raised from a trailing edge of the stack by means of a suction traverse. The sucked cardboard is pushed onto the subsequent alignment module 10 and the support lamp 8.
- the alignment module 10 has in this case so-called.
- Belt swords which form a transport ramp for the cardboard. The belt swords are swung to the level of the cartridge stack located in the magazine module 12. The belt swords convey the cardboard in the longitudinal direction against a stop of the alignment module 10, whereby a longitudinal alignment of the cardboard takes place.
- the belt swords are then lowered down below the level of transverse rollers of the alignment module 10.
- the cardboard comes to rest on the transverse rollers.
- the transverse rollers promote the cardboard against lateral stops of the alignment module 10, whereby a transverse orientation of the cardboard takes place.
- the parts to be packaged may be removed from the parts stack 18, eg by the industrial robot 16, and placed in the alignment module 10 on the oriented cardboard and the cardboard with the parts placed thereon on belt conveyors in the folding device 4 of the packaging center 2 be transported. There, the cardboard can then be sucked by pad suction of the folding device and is thus locked for folding in their position.
- the oriented cardboard could initially seized without applied parts by a cardboard gripper and then transported by belt conveyors in the folding device 4 and against attacks. The laying of the parts to be packaged on the cardboard can then be done within the packaging center 2 itself.
- corner flaps of the cardboard are then prefolded inwards. Furthermore, by folding up further folding flaps, the longitudinal sides of the cardboard are folded. Then a slide is extended to hold the long sides. Essentially, at the same time as the folding flaps are raised, cover sliders are extended which are positioned at the rear of the box. By means of further slides side flaps of the cardboard are folded. With the help of the folding flaps, the transverse sides of the cardboard are folded. By extending the slide the transverse sides are held. Subsequently, the folding flaps are then folded back longitudinally and transversely. A sub-box has now been created in which the parts to be packed are already located.
- the longitudinal sides of the prefabricated cardboard packaging are glued.
- the closure device 6 is moved from its provision position in the folding device 4 into its working position.
- a cover section of the cardboard is folded down forwards by means of a plurality of brackets.
- the lateral sides of the cardboard are glued by means arranged on the closure device 6 movable or adjustable HotMelt application nozzles.
- By extending a shutter slide longitudinal and transverse sides of cover tabs of the cardboard are folded down.
- By the aforementioned Machining steps creates an integral cardboard cover (top box), which closes the bottom carton.
- the counter-pressure bar of the closure device 6 is lowered onto the cardboard cover and held in this position until the hot-melt adhesive has cured. Once this is done, the shutter and the counter-pressure bar are moved upwards, and the shutter 6 is withdrawn from the area of the folder 4 back to its ready position.
- the finished cardboard package with the part (s) packaged therein is now removed from the packaging center 2 by means of the industrial robot 16 and stacked on the package stack 20.
- the finished carton pack can also be placed on belt conveyors or the like, e.g. be transported out of the packaging center 2 and then stacked accordingly on a transport path extending in extension of the alignment module 10.
- a purely manual removal is of course also possible.
- the device according to the invention may also assume a different form of construction than that described above.
- the device can in particular have features which are a combination of two or more of the respective ones Individual features of the accompanying claims.
- the packaging center was operated or loaded in the above example fully automatically with the help of an industrial robot as a handling device, it is of course also possible in a simple version of the device according to the invention to operate the packing center or its additional modules purely manually or to load.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Supplying Of Containers To The Packaging Station (AREA)
- Making Paper Articles (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
- Closing Of Containers (AREA)
- Buffer Packaging (AREA)
- Wrappers (AREA)
- Package Closures (AREA)
- Control And Other Processes For Unpacking Of Materials (AREA)
Description
- Die vorliegende Erfindung betrifft eine Verpackungsvorrichtung.
- Es sind Verpackungsvorrichtungen bekannt, die über eine oder mehrere stationär angeordnete Falteinrichtungen verfügen, die im Wesentlichen mit einem Stempel und einer Matrize ausgestattet sind. Ein zugeschnittener, plattenförmiger Verpackungsmaterialrohling wird in die Falteinrichtung eingelegt, mit einem Haftmittel versehen und zu einem Unterkarton gefaltet. Nach Entnahme des Unterkartons wird entweder mit Hilfe derselben Falteinrichtung oder einer zweiten Falteinrichtung und unter Verwendung eines weiteren Verpackungsmaterialrohlings auf die gleiche Art und Weise ein separater Oberkarton (hier: Deckel) hergestellt. Nach Fertigstellung von Ober- und Unterkarton wird manuell oder maschinell ein zu verpackender Gegenstand in den Unterkarton eingelegt und dann der Unterkarton mit dem darin verbindlichen Gegenstand durch Anbringen des Oberkartons verschlossen.
- Mit den zuvor beschriebenen Verpackungsvorrichtungen sind aufgrund der Tatsache, dass die jeweilige Falteinrichtung mit Stempel und Matrize arbeitet, die jeweils eine fixe, unveränderbare Abmessung besitzen, nur Verpackungen bzw.
- Kartons in einer einzigen Größe herstellbar. Für eine andere Verpackungsgröße müssten Stempel und Matrize gegen einen neuen Stempel und eine neue Matrize mit einer anderen Abmessung ausgetauscht werden. Sowohl die Herstellung verschiedener Stempel und Matrizen als auch das jeweilige Umrüsten der Verpackungsvorrichtung ist jedoch kostenintensiv, aufwendig und insbesondere bei kleinere Serien unwirtschaftlich. Zur Herstellung von Oberkarton und Unterkarton sind zudem entweder zwei verschiedene Falteinrichtungen oder zwei gänzlich voneinander getrennte Herstellungsabschnitte mit zusätzlichen Schritten für die Entnahme des zuerst gefertigten Unterkartons, zum Einlegen des Verpackungsmaterialrohlings, der Herstellung des Oberkartons und dessen Entnahme aus der Vorrichtung erforderlich. Ferner kann der zu verpackende Gegenstand erst dann in den Unterkarton eingelegt werden, wenn zumindest die Fertigung des Unterkartons vollständig abgeschlossen und der Stempel aus dem Unterkarton entfernt ist. Der gesamte Verpackungsprozess ist daher vergleichsweise langwierig und aufwendig.
- Es sind deshalb Verpackungsvorrichtungen entwickelt worden, die im Durchlaufverfahren arbeiten. Ein zugeschnittener, und beispielsweise einteiliger, plattenförmiger Verpackungsmaterialrohling, aus dem sowohl ein Unterkarton als auch ein integraler Oberkarton faltbar ist, wird mit einem auf die Rohlingoberfläche platzierten zu verpackenden Gegenstand oder Teil auf eine Durchlaufstrecke aufgelegt und einer Falteinrichtung zugeführt. In der Falteinrichtung werden Abschnitte des Verpackungsmaterialrohlings mit einem Haftmittel versehen; ferner werden mittels Faltelementen Abschnitte des Verpackungsmaterialrohlings um den zu verpackenden Gegenstand herum gefaltet werden, so dass ein Unterkarton entsteht, in dem der Gegenstand bereits teilweise verpackt ist. Anschließend wird der Unterkarton mit dem darin befindlichen Gegenstand in Durchlaufrichtung zu einer von der Falteinrichtung örtlich getrennten bzw. räumlich beabstandeten Verschlusseinrichtung transportiert. Dort werden weitere Abschnitte des Verpackungsmaterialrohlings mit einem Haftmittel versehen, und mittels Verschlusselementen wird aus dem gleichen Verpackungsmaterialrohling ein Oberkarton gefaltet und über dem Unterkarton verschlossen, wodurch der Gegenstand nun vollständig verpackt ist.
- Bei den zuvor genannten, nach dem Durchlaufprinzip arbeitenden Verpackungsvorrichtungen sind die Falt- und Verschlusselemente üblicherweise größenverstellbar ausgebildet, so dass ohne größere Umrüstarbeiten auch Verpackungen unterschiedlichster Größe herstellbar sind. Aufgrund des Durchlaufprinzips sowie der damit zusammenhängenden räumlich getrennten Anordnung von Falt- und Verschlusseinrichtung haben derartige Vorrichtungen jedoch eine voluminöse Bauweise und erfordern eine sehr große Aufstellfläche. Auch sind extra Transporteinrichtungen vorzusehen, welche den Unterkarton bzw. die halbfertige Verpackung von der Falteinrichtung zu der Verschlusseinrichtung überführen. Infolge des Durchlaufprinzips und der damit vorgegebenen festen Anordnung der Falt- und Verschlusseinrichtung, der Transporteinrichtung sowie weiterer ggf. vor- oder nachgeschalteter Zusatzeinrichtungen ist dieses Vorrichtungskonzept auch nicht ohne weitere abzuändern oder an die jeweiligen Zusatzeinrichtungen anzupassen.
- Ferner offenbart die EP 0 983 940 A eine Verpackungsvorrichtung nach dem Oberbegriff von Anspruch 1.
- Der Erfindung liegt die Aufgabe beziehungsweise das technische Problem zugrunde, eine neuartige Verpackungseinrichtung zu schaffen, welche die dem Stand der Technik anhaftenden Nachteile weitmöglichst vermeidet und sowohl ein vergleichsweise einfaches und effektives Verpacken eines Gegenstandes gewährleistet als auch leichter an variierende Fertigungssituationen anpassbar ist.
- Diese Aufgabe wird gelöst durch eine erfindungsgemäße Verpackungsvorrichtung mit den Merkmalen des Anspruchs 1. Diese Verpackungsvorrichtung, umfasst ein einzelnes, stationär angeordnetes, modular erweiterbares Verpackungscenter mit einer integrierten, stempel- und matrizenfreien Falt- und Verschlusseinrichtung mit größenverstellbaren Falt-, Verschluss- und Haftmittelauftragselementen.
- Die Falt- und die Verschlusseinrichtung gehören bei der erfindungsgemäßen Verpackungsvorrichtung unmittelbar funktional zusammen. Bei der erfindungsgemäßen Verpackungsvorrichtung werden, anders als bei den nach dem Durchlaufprinzip arbeitenden Vorrichtungen, sämtliche für das Verpacken eines jeweiligen Gegenstandes erforderlichen Schritte, d.h. das Auftragen eines Haftmittels auf den Verpackungsmaterialrohling, das Falten des Verpackungsmaterialrohlings zu einem Unterkarton, der den zu verpackenden Gegenstand bereits enthalten kann, und das Verschließen des Unterkartons durch einen vorzugsweise aus dem selben Verpackungsmaterialrohling gefalteten Oberkarton in einem einzelnen, einheitlichen, stationär angeordneten Verpackungscenter ausgeführt.
- Die erfindungsgemäße Verpackungsvorrichtung ist dadurch nicht nur sehr kompakt und raumsparend, sie bedarf auch keiner extra Transporteinrichtung, um die halbfertige Verpackung von der Falteinrichtung zu der Verschlusseinrichtung zu überführen. Der Verpackungsrohling kann vielmehr stationär an einer einzigen Bearbeitungsposition bearbeitet und der Gegenstand an dieser Position verpackt werden. Dies ist nicht nur dann vorteilhaft, wenn die erfindungsgemäße Vorrichtung manuell bedient wird, da für nahezu sämtliche Bedienungsaktivitäten nur eine einzige Person an einem einzigen Ort erforderlich ist, sondern auch dann, wenn die Vorrichtung beispielsweise zum Zwecke der weiteren Automatisierung durch zusätzliche Vorrichtungskomponenten, wie zum Beispiel Roboter, erweitert werden soll.
- Da die erfindungsgemäße Verpackungsvorrichtung ähnlich wie die nach dem Durchlaufprinzip arbeitenden Vorrichtungen zudem mit einer stempel- und matrizenfreien Falt- und Verschlusseinrichtung mit größenverstellbaren Falt-, Verschluss- und Haftmittelauftragselementen ausgestattet ist, die jedoch allesamt von dem einzelnen Verpackungscenter umfasst sind, ist die erfindungsgemäße Verpackungsvorrichtung trotz der stationären Anordnung des Verpackungscenters zur Herstellungen von Verpackungen unterschiedlichster Größe geeignet. Aufwendige Umrüstarbeiten oder dergleichen sind hierzu nicht erforderlich. Auch Kleinserien sind effektiv und wirtschaftlich zu fertigen.
- Wie bereits zuvor angedeutet, kann sich der zu verpackende Gegenstand bei der Herstellung seiner Umverpackung bereits auf dem Verpackungsmaterialrohling angeordnet befinden, wodurch eine weitere Rationalisierung und eine hohe Verpackungsgeschwindigkeit erzielt wird.
- Weil bei der erfindungsgemäßen Verpackungsvorrichtung sämtliche, für den eigentlichen Verpackungsvorgang wesentlichen Vorrichtungskomponenten in einem einzelnen, modular erweiterbaren Verpackungscenter konzentriert sind, das gewissermaßen eine autonome Funktionseinheit bildet, lässt sich die erfindungsgemäße Verpackungsvorrichtung auch besonders einfach, ohne großen Aufwand und äußerst flexibel mit etwaigen anderen, zusätzlichen Vorrichtungskomponenten kombinieren und leicht an unterschiedlichste Fertigungssituationen anpassen.
- Weitere bevorzugte und vorteilhafte Ausgestaltungsmerkmal der erfindungsgemäßen sind Gegenstand der Unteransprüche.
- Ein bevorzugtes Ausführungsbeispiel der Erfindung mit zusätzlichen Ausgestaltungsdetails ist nachfolgend unter Bezugnahme auf die beigefügte Zeichnung näher beschrieben und erläutert.
- Die Figur zeigt eine schematische Draufsicht auf eine erfindungsgemäße Verpackungsvorrichtung mit weiteren zusätzlichen Vorrichtungsmodulen.
- In der beigefügten Figur ist eine schematische Draufsicht auf eine erfindungsgemäße Verpackungsvorrichtung mit weiteren zusätzlichen Vorrichtungsmodulen dargestellt. Die erfindungsgemäße Verpackungsvorrichtung, umfasst ein einzelnes, stationär angeordnetes, modular erweiterbares, Verpackungscenter 2 mit einer integrierten, stempel- und matrizenfreien Falteinrichtung 4 sowie einer Verschlusseinrichtung 6 mit größenverstellbaren Falt-, Verschluss- und Haftmittelauftragselementen. Das Verpackungscenter 2 bildet eine Art einzelner "Verpackungszelle". Die Falteinrichtung 4 und die Verschlusseinrichtung 6 sind im vorliegenden Ausführungsbeispiel an einem gemeinsamen Gestell des Verpackungscenters 2 angeordnet. Bei den Faltelementen kann es sich beispielsweise um Schieber und/oder Faltklappen, bei den Verschlusselementen um Verschlussschieber und/oder Gegendruckbalken und/oder Bügel, und bei den Haftmittelauftragselementen um Auftragsdüsen oder dergleichen handeln. Mit den Auftragsdüsen kann beispielsweise ein Haftmittel in der Form eines Schmelzklebers (HotMelt-Kleber, o.ä. Mittel) aufgetragen werden.
- Wie in der Figur erkennbar, und wie durch Doppelpfeile angedeutet, ist die Verschlusseinrichtung 6 von einer zumindest teilweise neben der Falteinrichtung 4 befindlichen Bereitstellungsposition in die Falteinrichtung 4 hinein in eine Arbeitsposition und aus dieser wieder zurück verfahrbar.
- Die Verpackungsvorrichtung umfasst ferner ein mit einer Auflagerampe 8 ausgestattetes Verpackungsmaterial-Ausrichtmodul 10, das an einer in der Zeichnung linken Seite des Verpackungscenters 2 angeordnet und modular mit dem Verpackungscenter 2 gekoppelt bzw. kombiniert ist. Das Ausrichtmodul 10 fungiert im vorliegenden Beispiel gleichzeitig als Verpackungsmaterial-Beschickungsmodul.
- An der linken Seite des Ausrichtmoduls 10 wiederum ist ein Verpackungsmaterial-Magazinmodul 12 angeordnet, dass modular mit dem Ausrichtmodul 10 und über dieses wiederum mit dem Verpackungscenter 2 gekoppelt bzw. kombiniert ist.
- Ein Teile-Beschickungs- und Entnahmemodul 14 zum Beschicken des stationären Verpackungscenters 2 mit zu verpackenden Teilen ist im vorliegenden Ausführungsbeispiel links vor dem Verpackungscenter 2 angeordnet und modular mit dieser kombiniert. Das Teile-Beschickungs- und Entnahmemodul 14 umfasst hier einen Industrieroboter 16, welcher die zu verpackenden Teile von einem Teilestapel 18 entnimmt, im Bereich des Ausrichtmoduls 10 auf das Verpackungsmaterial auflegt und später die fertig verpackten Teile samt ihrer Verpackung wieder aus dem Verpackungscenter 2 entnimmt und zu einem Paketstapel 20 zusammenstellt.
- Es werden nun der Betrieb der erfindungsgemäßen Vorrichtung sowie weitere Vorrichtungsdetails beschrieben werden.
- Für das vorliegende Beispiel wird angenommen, dass es sich bei dem Verpackungsmaterial, mit dem Teile oder Gegenstände verpackt werden sollen, um einen Kartonrohling nach dem Standard Fefco 04110 handelt. Der Kartonrohling wird nachfolgend kurz Kartonage genannt werden. Die Erfindung ist jedoch selbstverständlich nicht auf dieses Verpackungsmaterial und den besagten Standard beschränkt. Grundsätzlich können mit der erfindungsgemäßen Vorrichtung auch andere geeignete Verpackungsmaterialien bzw. Kartonagen bearbeitet werden.
- Zunächst wird das Magazinmodul 12 mit einem Kartonagestapel aufgefüllt. Dann wird eine Kartonage von einer Hinterkante des Stapels her mittels einer Saugertraverse angehoben. Die angesaugte Kartonage wird auf das nachfolgende Ausrichtmodul 10 und die Auflagerampe 8 geschoben. Das Ausrichtmodul 10 besitzt in diesem Fall sog. Riemenschwerter, die eine Transportrampe für die Kartonage bilden. Die Riemenschwerter sind auf das Niveau des im Magazinmodul 12 befindlichen Kartonagestapels ausgeschwenkt. Die Riemenschwerter fördern die Kartonage in Längsrichtung gegen einen Anschlag des Ausrichtmoduls 10, wodurch eine Längsausrichtung der Kartonage erfolgt.
- Die Riemenschwerter werden danach nach unten unter das Niveau von Querrollen des Ausrichtmoduls 10 abgesenkt. Dadurch kommt die Kartonage auf den Querrollen zu liegen. Die Querrollen fördern die Kartonage gegen seitliche Anschläge des Ausrichtmoduls 10, wodurch eine Querausrichtung der Kartonage erfolgt.
- Danach gibt es zwei verschiedene mögliche Wege des weiteren Arbeitsablaufs. Erstens können die zu verpackenden Teile, wie im vorliegenden Beispiel, z.B. mittels des Industrieroboters 16 von dem Teilestapel 18 genommen und noch in dem Ausrichtmodul 10 auf die ausgerichtete Kartonage gelegt und die Kartonage mit den darauf aufgelegten Teilen auf Riemenförderern in die Falteinrichtung 4 des Verpackungscenters 2 eintransportiert werden. Dort kann die Kartonage dann durch Auflagesauger der Falteinrichtung angesaugt werden und ist damit für das Falten in ihrer Lage arretiert. Zweitens könnte die ausgerichtete Kartonage zunächst auch ohne aufgelegte Teile durch einen Kartonagegreifer ergriffen und dann mit Hilfe von Riemenförderern in die Falteinrichtung 4 und gegen Anschläge transportiert werden. Das Auflegen der zu verpackenden Teile auf die Kartonage kann dann innerhalb des Verpackungscenters 2 selbst erfolgen.
- Durch Hochfahren von Faltklappen der Falteinrichtung 4 werden dann Ecklaschen der Kartonage nach innen vorgefaltet. Ferner werden durch Hochfahren weiterer Faltklappen die Längsseiten der Kartonage gefaltet. Dann wird ein Schieber zum Halten der Längsseiten ausgefahren. Im Wesentlichen gleichzeitig mit dem Hochfahren der Faltklappen werden Deckelschieber ausgefahren, die an der Hinterseite des Kartons positioniert sind. Mittels weiterer Schieber werden Seitenlaschen der Kartonage eingeklappt. Mit Hilfe der Faltklappen werden die Querseiten der Kartonage gefaltet. Durch Ausfahren der Schieber werden die Querseiten gehalten. Anschließend werden die Faltklappen dann wieder längs und quer zurückgeklappt. Es ist nun ein Unterkarton entstanden, in dem sich bereits die zu verpackenden Teile befinden.
- Mittels der verfahrbaren, bzw. verstellbaren HotMelt-Auftragsdüsen des Verpackungscenters 2 werden die Längsseiten der so vorgefertigten Kartonage beleimt.
- Nun wird die Verschlusseinrichtung 6 von ihrer Bereitstellungsposition in die Falteinrichtung 4 hinein in ihre Arbeitsposition gefahren. Im Wesentlichen gleichzeitig wird mittels mehrerer Bügel ein Deckelabschnitt der Kartonage nach vorn herunter gefaltet. Dann werden mittels an der Verschlusseinrichtung 6 angeordneter verfahrbarer, bzw. verstellbarer HotMelt-Auftragsdüsen die Querseiten der Kartonage beleimt. Durch Ausfahren eines Verschlussschiebers werden Längs- und Querseiten von Deckellaschen der Kartonage herunter gefaltet. Durch die vorher genannten Bearbeitungsschritte entsteht ein integraler Kartondeckel (Oberkarton), welcher den Unterkarton verschließt.
- Im wesentlichen gleichzeitig mit dem Ausfahren des Verschlussschiebers wird der Gegendruckbalken der Verschlusseinrichtung 6 auf den Kartondeckel abgesenkt und in dieser Position gehalten, bis der HotMelt-Kleber ausgehärtet ist. Sobald dies geschehen ist, werden der Verschlussschieber und der Gegendruckbalken nach oben gefahren, und die Verschlusseinrichtung 6 wird aus dem Bereich der Falteinrichtung 4 heraus wieder zurück in ihre Bereitstellungsposition zurückgezogen.
- Das fertige Kartonpaket mit den darin verpackten Teil(en) wird nun mittels des Industrieroboters 16 dem Verpackungscenter 2 entnommen und auf dem Packungsstapel 20 abgestapelt .
- Nach Absenken der Faltklappen und Schieber kann das fertige Kartonpaket aber auch auf Riemenförderern oder dergleichen, z.B. auf einer sich in Verlängerung des Ausrichtmoduls 10 erstreckenden Transportstrecke, aus dem Verpackungscenter 2 heraus transportiert und dann entsprechend abgestapelt werden. Eine rein manuelle Entnahme ist selbstverständlich ebenso möglich.
- Für eine Kartonage ist der Bearbeitungszyklus nun abgeschlossen. Für nachfolgende Kartonagen ist der Bearbeitungsablauf entsprechend.
- Die Erfindung ist nicht auf die obigen Ausführungsbeispiele, die lediglich der allgemeinen Erläuterung des Kerngedankens der Erfindung dienen, beschränkt. Im Rahmen des Schutzumfangs kann die erfindungsgemäße Vorrichtung vielmehr auch eine andere als die oben beschriebene Ausgestaltungsform annehmen. Die Vorrichtung kann hierbei insbesondere Merkmale aufweisen, die eine Kombination aus zwei oder mehreren der jeweiligen Einzelmerkmale der beiliegenden Ansprüche darstellen. Obwohl das Verpackungscenter in dem obigen Beispiel voll automatisch mit Hilfe eines Industrieroboters als Handlinggerät bedient bzw. beschickt wurde, ist es in einer Einfachversion der erfindungsgemäßen Vorrichtung natürlich ebenso möglich, das Verpackungscenter bzw. dessen Zusatzmodule rein manuell zu bedienen bzw. zu beschicken.
- Bezugszeichen in den Ansprüchen, der Beschreibung und den Zeichnungen dienen lediglich dem besseren Verständnis der Erfindung und sollen den Schutzumfang nicht einschränken.
Claims (5)
- Verpackungsvorrichtung, umfassend
ein einzelnes, stationär angeordnetes, modular erweiterbares Verpackungscenter (2) mit einer integrierten, stempel- und matrizenfreien Falt- (4) und Verschlusseinrichtung (6) mit größenverstellbaren Falt-, Verschluss- und Haftmittelauftragselementen,
dadurch gekennzeichnet, dass die Verschlusseinrichtung (6) linear von einer zumindest teilweise neben der Falteinrichtung (4) befindlichen Bereitstellungsposition in die Falteinrichtung (4) hinein in eine Arbeitsposition und wieder zurück verfahrbar ist. - Verpackungsvorrichtung nach Anspruch 1,
dadurch gekennzeichnet, dass
diese ein Verpackungsmaterial-Beschickungsmodul (10) umfasst, welches mit dem Verpackungscenter (2) modular kombinierbar ist. - Verpackungsvorrichtung nach einem oder mehreren der vorher genannten Ansprüche,
dadurch gekennzeichnet, dass
diese ein Verpackungsmaterial-Ausrichtmodul (10) umfasst, welches mit dem Verpackungscenter (2) und/oder dem Verpackungsmaterial-Beschickungsmodul modular kombinierbar ist. - Verpackungsvorrichtung nach einem oder mehreren der vorher genannten Ansprüche,
dadurch gekennzeichnet, dass
diese ein Verpackungsmaterial-Magazinmodul (12) umfasst, welches mit dem Verpackungscenter (2) und/oder dem Verpackungsmaterial-Beschickungsmodul (10) und/oder dem Verpackungsmaterial-Ausrichtmodul (10) modular kombinierbar ist. - Verpackungsvorrichtung nach einem oder mehreren der vorher genannten Ansprüche,
dadurch gekennzeichnet, dass
diese ein Teile-Beschickungs- und Entnahmemodul (14, 16) umfasst, welches modular mit dem Verpackungscenter (2) kombinierbar ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10123356 | 2001-05-14 | ||
| DE10123356A DE10123356A1 (de) | 2001-05-14 | 2001-05-14 | Verpackungsvorrichtung |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1260444A2 EP1260444A2 (de) | 2002-11-27 |
| EP1260444A3 EP1260444A3 (de) | 2003-04-23 |
| EP1260444B1 true EP1260444B1 (de) | 2007-03-07 |
Family
ID=7684700
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02005348A Expired - Lifetime EP1260444B1 (de) | 2001-05-14 | 2002-03-14 | Verpackungsvorrichtung |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP1260444B1 (de) |
| AT (1) | ATE356030T1 (de) |
| DE (2) | DE10123356A1 (de) |
| DK (1) | DK1260444T3 (de) |
| ES (1) | ES2282336T3 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1645513A3 (de) * | 2004-09-21 | 2006-04-19 | Philip Morris Products S.A. | Modulares Verpackungssystem |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2123991A1 (de) * | 1971-02-04 | 1972-08-17 | Canadian International Paper Co., Montreal, Quebec (Kanada) | Verpackungsmaschine |
| US4067172A (en) * | 1977-01-28 | 1978-01-10 | Excel Engineering, Inc. | Carton set-up and loading machine |
| US4569184A (en) * | 1981-11-06 | 1986-02-11 | Anderson Bros Apv Inc | Machine for erecting, filling and closing cartons |
| IT1235924B (it) * | 1989-11-07 | 1992-12-02 | Cestind Centro Studi Ind | Macchina per confezionare prodotti in generale allestendo astucci o scatole del tipo detto a coperchio incernierato (hinged-lid) chiudibile su collarino a sigillo di garanzia partendo da singoli sbozzati piani a parti componenti multiple |
| IE894213A1 (en) * | 1989-12-29 | 1991-07-03 | Oseney Ltd | Packaging and treatment of food products |
| DE4314686C1 (de) * | 1993-05-04 | 1994-09-22 | Uhlmann Pac Systeme Gmbh & Co | Magazinvorrichtung mit Antriebsspindeln zur Formatanpassung des Magazinschachts |
| DE19860018A1 (de) * | 1997-12-30 | 1999-07-08 | Tmc Spa | Verpackungsautomat zur Konfektionierung von Produkten |
| DE19840077C2 (de) * | 1998-09-03 | 2003-12-11 | Winkler & Duennebier Ag | Vorrichtung zum Verpacken von Gegenständen oder von Stapeln |
| GB9928230D0 (en) * | 1999-12-01 | 2000-01-26 | Bradman Lake Ltd | Robotic end-loader |
| DE19962302A1 (de) * | 1999-12-23 | 2001-09-06 | Winkler & Duennebier Ag | Verfahren und Vorrichtung zum Verpacken von flachen Gegenständen |
-
2001
- 2001-05-14 DE DE10123356A patent/DE10123356A1/de not_active Ceased
-
2002
- 2002-03-14 AT AT02005348T patent/ATE356030T1/de not_active IP Right Cessation
- 2002-03-14 DK DK02005348T patent/DK1260444T3/da active
- 2002-03-14 EP EP02005348A patent/EP1260444B1/de not_active Expired - Lifetime
- 2002-03-14 ES ES02005348T patent/ES2282336T3/es not_active Expired - Lifetime
- 2002-03-14 DE DE50209628T patent/DE50209628D1/de not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| DK1260444T3 (da) | 2007-07-02 |
| DE10123356A1 (de) | 2002-11-28 |
| EP1260444A2 (de) | 2002-11-27 |
| ES2282336T3 (es) | 2007-10-16 |
| DE50209628D1 (de) | 2007-04-19 |
| ATE356030T1 (de) | 2007-03-15 |
| EP1260444A3 (de) | 2003-04-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE60222180T2 (de) | Maschine zur verpackung von flaschen in pappkartons | |
| DE69604380T2 (de) | Verpackungsvorrichtung für aufgestapelte papiererzeugnisse | |
| DE19840077A1 (de) | Verfahren und Vorrichtung zum Verpacken von Gegenständen | |
| EP3372516B1 (de) | Verpackungsvorrichtung und verfahren zum aufsetzen einzelner artikel oder zusammenstellungen an artikeln auf flächige verpackungszuschnitte | |
| DE19517798A1 (de) | Verfahren zum Herstellen von Zigarettenkartons mit starrer Klappdeckelverpackung | |
| EP3808668B1 (de) | Vorrichtung zum umgang mit zu verpackenden artikeln und verfahren zum anpassen einer vorrichtung für den transport von zum verpacken vorgesehenen artikeln | |
| DE4035352A1 (de) | Vorrichtung zum herstellen von schachteln und zum verpacken von produkten in diese | |
| EP2602204A1 (de) | Karton zum Verpacken von beutelartigen Getränkebehältnissen, Maschine zum Verschließen einer Verpackung und Verfahren zum Verschließen einer Verpackung | |
| EP3372513B1 (de) | Vorrichtung zum umgang mit artikeln sowie verfahren zum tauschen mindestens eines transportmoduls und wenigstens eines arbeitsmoduls der vorrichtung | |
| EP4482769A1 (de) | Verpackungsanlage und verfahren zur zuführung von flächigen verpackungsmitteln zu einer verpackungsanlage | |
| DE4338799A1 (de) | Verpackung für Bücher und/oder andere Produkte sowie Verfahren und Vorrichtung zu ihrer Herstellung | |
| DE3421261A1 (de) | Vorrichtung zum falten und verschliessen der stirnwaende von tray-kartons | |
| EP4112486A1 (de) | Verpackungsmagazin für einen manipulator und verpackungssystem zum herstellen von gebinden | |
| DE2336163A1 (de) | Verfahren zum herstellen von packungen unter verwendung zweier zuschnitte | |
| EP2739552A1 (de) | Packung für zigaretten | |
| DE2636320C2 (de) | Vorrichtung zum automatischen Palettieren von Gegenständen, insbesondere Flaschen | |
| DE4018024A1 (de) | Verfahren und vorrichtung zum verpacken von beuteln | |
| DE102017008337A1 (de) | Verfahren und Vorrichtung zum Herstellen von Zigarettenpackungen | |
| DE2612458C2 (de) | Verfahren zum Aufrichten und Verkleben von zunächst ebenen, mit Falzlinien und Klebeflächen versehenen Kartonzuschnitten und zum Verpacken von Behältern in den entstehenden Kartons | |
| EP2391553B1 (de) | Verfahren zum erstellen einer paletteneinheit sowie paletteneinheit | |
| EP4514707A1 (de) | Verpackungsvorrichtung und verfahren zum anbringen eines verpackungsmittels an eine artikelzusammenstellung | |
| EP1260444A2 (de) | Verpackungsvorrichtung | |
| WO2023280539A1 (de) | Verpackungsmaschine und verfahren zur herstellung von verpackungseinheiten | |
| DE2540769A1 (de) | Vorrichtung zur automatischen herstellung einer unverletzlichen verpackung fuer einen rechtwinkeligen inhalt | |
| DE102013011884A1 (de) | Verfahren und Vorrichtung zur Herstellung von Packungen für Zigaretten |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: 7B 65B 5/02 B Ipc: 7B 65B 59/04 A |
|
| 17P | Request for examination filed |
Effective date: 20030620 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| 17Q | First examination report despatched |
Effective date: 20041202 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070307 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070307 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 50209628 Country of ref document: DE Date of ref document: 20070419 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070807 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20070307 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2282336 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| EN | Fr: translation not filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070307 |
|
| BERE | Be: lapsed |
Owner name: LIGMATECH AUTOMATIONSSYSTEME G.M.B.H. Effective date: 20070331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070331 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070331 |
|
| 26N | No opposition filed |
Effective date: 20071210 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070331 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070608 Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20071026 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070314 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070307 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070307 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070314 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DK Payment date: 20110325 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20110307 Year of fee payment: 10 Ref country code: SE Payment date: 20110324 Year of fee payment: 10 Ref country code: FI Payment date: 20110321 Year of fee payment: 10 Ref country code: IT Payment date: 20110314 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20110228 Year of fee payment: 10 Ref country code: DE Payment date: 20110325 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120314 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120315 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50209628 Country of ref document: DE Effective date: 20121002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120314 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120331 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20130710 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120315 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120314 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121002 |