EP0509665A2 - Verfahren und Vorrichtung zum Schleifen des Endes eines rohrförmigen Werkstückes - Google Patents
Verfahren und Vorrichtung zum Schleifen des Endes eines rohrförmigen Werkstückes Download PDFInfo
- Publication number
- EP0509665A2 EP0509665A2 EP92302772A EP92302772A EP0509665A2 EP 0509665 A2 EP0509665 A2 EP 0509665A2 EP 92302772 A EP92302772 A EP 92302772A EP 92302772 A EP92302772 A EP 92302772A EP 0509665 A2 EP0509665 A2 EP 0509665A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- workpiece
- tool
- carriage
- holding means
- arm
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000000034 method Methods 0.000 title claims description 14
- 239000012530 fluid Substances 0.000 claims description 10
- 230000006835 compression Effects 0.000 claims description 5
- 238000007906 compression Methods 0.000 claims description 5
- 238000003825 pressing Methods 0.000 claims 1
- 238000005266 casting Methods 0.000 description 6
- 239000002184 metal Substances 0.000 description 4
- 230000002787 reinforcement Effects 0.000 description 3
- 238000009987 spinning Methods 0.000 description 3
- 239000003638 chemical reducing agent Substances 0.000 description 1
- 238000000605 extraction Methods 0.000 description 1
- 238000003780 insertion Methods 0.000 description 1
- 230000037431 insertion Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- NJPPVKZQTLUDBO-UHFFFAOYSA-N novaluron Chemical compound C1=C(Cl)C(OC(F)(F)C(OC(F)(F)F)F)=CC=C1NC(=O)NC(=O)C1=C(F)C=CC=C1F NJPPVKZQTLUDBO-UHFFFAOYSA-N 0.000 description 1
- 239000011236 particulate material Substances 0.000 description 1
- 239000011819 refractory material Substances 0.000 description 1
- 230000003014 reinforcing effect Effects 0.000 description 1
- 229910010271 silicon carbide Inorganic materials 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B27/00—Other grinding machines or devices
- B24B27/0084—Other grinding machines or devices the grinding wheel support being angularly adjustable
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B27/00—Other grinding machines or devices
- B24B27/0046—Column grinding machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B9/00—Machines or devices designed for grinding edges or bevels on work or for removing burrs; Accessories therefor
- B24B9/007—Machines or devices designed for grinding edges or bevels on work or for removing burrs; Accessories therefor for end faces of tubes
Definitions
- This invention relates to an improved method and apparatus for finishing the end of a tubular workpiece, and more particularly to a method and apparatus wherein a finishing tool is pivotable outwardly to permit insertion of a tubular workpiece into a rotatable holder.
- bottom pressure casting There is a known technique for casting articles from molten metal, commonly referred to as bottom pressure casting, wherein molten metal in an enclosed ladle is pressurized and forced upwardly through a refractory pouring tube and into the bottom of a mold.
- molten metal in an enclosed ladle is pressurized and forced upwardly through a refractory pouring tube and into the bottom of a mold.
- the pouring tube itself must be frequently replaced but is normally usable to successively supply a large number of molds.
- the upper end of the pouring tube must closely fit the mold bottom to prevent leakage of molten metal at that juncture and is preferably chamfered.
- pouring tubes are sizeable pieces of equipment. For instance in an installation for casting railcar wheels the pouring tubes are 6 1/2 inches in diameter and several feet long.
- the tube ends have been finished by hand held grinders.
- it has been difficult to position such a workpiece for end finishing; and it has also been difficult to properly posture and maintain a finishing tool to obtain an accurate chamfered end on the workpiece.
- the present invention involves the inserting of a tubular workpiece in an axial direction into an annular holder, pivoting a finishing tool, in a direction preferably radial to the holder, and workpiece to a posture over the workpiece, extending the finishing tool in a generally longitudinal direction against the workpiece end while rotating the workpiece about its longitudinal axis and thereafter withdrawing and pivoting the tool in an opposite direction to permit extraction of the workpiece in an axial direction from the annular holder.
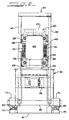
- a preferred apparatus to perform the foregoing steps comprises an upstanding base with an annular workpiece holder rotatably mounted on the base, a carriage pivotally mounted to one side of the base for pivotal movement substantially radially of the annular holder, tool means reciprocally mounted on the carriage, and power means connected between the base and carriage to pivot the latter.
- the preferred embodiment of the invention was devised to finish the end of a six and one half inch (6 1/2") diameter molten metal pouring tube 10, made of a refractory material, and thereby provide an accurate planar inner end edge with a slight chamfer downward from the inside tube surface to the outside surface.
- the finishing tool is a carborundum grinding disk generally 20 having a flat circular abrasive face 22 that is spun at high speed about the disk axis.
- the devised method begins with positioning the pouring tube 10 by inserting it into an annular holder generally 30 and then rotating the tube 10 about its axis. After inserting the tube 10 the finishing tool is operatively located by moving it inwardly from an inoperative posture, to one side of the tube 10, in a direction radial to the tube axis to an operative posture with the finishing tool opposing but spaced from the tube end; while simultaneously exerting a biasing force to move the tool away from the tube end.
- the tool is moved radially into the operative posture by swinging or pivoting it about a point to one side of the tube 10 and in a plane containing the axis of the tube so as to maintain the axis of the grinding disk 20 in that plane and thereby assure that the abrasive face 22 is maintained perpendicular to a plane containing the tube axis.
- the swinging or pivoting movement of the tool also enables limiting the inward movement and thereby placing the axis of the tool at a slight angle to the axis of the tube 10 at the operative posture, which angle will establish the chamfer placed on the finished tube end.
- the procedure is then continued by extending the tool into contact with the tube end while both rotating the tube 10 and spinning the grinding disk 20.
- the tool is extended by applying fluid pressure sufficient to overcome the aforementioned biasing force and to urge the tool against the tube end.
- fluid pressure sufficient to overcome the aforementioned biasing force and to urge the tool against the tube end.
- the rotating of the tube and spinning of the tool are continued at least until the pressure becomes constant thereby indicating that an even finish of the workpiece end has been achieved.
- the procedure is concluded by terminating the fluid pressure overcoming the biasing force, thereby withdrawing the tool away from the tube end, then returning the tool to the inoperative posture by swinging or pivoting it in the axial plane, and finally extracting the tube 10 in an axial direction from the annular holder 30.
- a preferred apparatus for carrying out the method includes an upstanding fixed frame generally 40 supported on a floor 42 or the like.
- the frame has a top 44 with a circular opening 46.
- Concentric with the opening 46 are an annular bearing raceway 48 and an annular ring gear 50 supported therein.
- the annular holder generally 30 is secured to the ring gear 50 and includes a chuck 52 to center and secure the pouring tube generally 10, including parting ring 12 and holding casting 14, therein.
- the floor beneath the fixed frame 40 may also have an opening directly beneath circular opening 46 in frame top 44 to permit the processing of long workpieces.
- An electric motor 60 is fastened to the frame 40 and a gear reducer 62 connects the motor shaft to the annular ring gear 50 to cause the latter to rotate in the raceway 48 and thereby rotate any workpiece centered in the chuck 52 about the workpiece axis.
- a flat base or pedestal 70 rests on the floor 42 immediately to one side of the fixed frame 40.
- a pair of spaced trunnions 72, 74 are slidingly supported on the base 70 for adjustment toward and away from the fixed frame 40; and a pivot shaft or axle 80 is rotatably held in the trunnions 72, 74 to be perpendicular to the axis of rotation of both the ring gear 50 and workpiece, and also perpendicular to a radius of the workpiece that bisects the shaft 80.
- Threaded bolts 82, 84 extend through the respective trunnions 72, 74 and into the fixed frame 40.
- a plurality of adjustable nuts 86 on the bolts 82, 84 provide for accurately positioning and securing the trunnions, 72 74 with respect to the frame 40.
- a pivotable carriage generally 90 comprising a pair of upstanding channel members 92, 94 and one or more cross members 90 fixed to the channels, is supported on the shaft 80 so as to be pivotable toward and away from the fixed frame 40.
- Each respective channel member 92, 94 is connected to the shaft 90 closely adjacent a trunnion 72, 74; and a power cylinder 100 is fastened centrally to a cross member 96 with its reciprocal rod 102 extending toward the fixed frame 40 where it is connected by a clevis 104 and pin 106.
- the clevis 104 is detachably fastened to the frame 40 so that a selectable shim 110 is insertable therebetween.
- a movable platform generally 120 is carried between the channel members 92, 94 of carriage 90 at a level above the chuck 52 and workpiece therein.
- the platform 120 includes a cross arm 122 that extends between and is perpendicular to the channels 92, 94 and a depending plate 124 fastened to the underside of cross arm 122 and extending parallel to the channels.
- Four casters 128 bolted to the channels 92, 94 engage opposite edges of the plate 124 and confine its movement to parallel the channels.
- Compression springs 132, 134 are secured between brackets 138, 140 on each edge of the plate 124 and opposing brackets 142, 144 fastened to the respective channels 92, 94 and bias the platform 120 upwardly.
- a beam 150 extends beneath cross arm 122 from the center of one side of the depending plate 124 to a cylindrical casing 152 at the end over the fixed frame 40.
- An electric tool driving motor 156 is mounted to the opposite side of the depending plate 124 with its drive shaft 158 and drive pulley 160 disposed upwardly.
- a tool drive shaft 162 extends through the casing 152 and a pulley 164 thereon is drivingly connected to the motor pulley 160 by a belt 166. It is important that the tool drive shaft 162 is aligned to be maintained in a plane that contains the workpiece axis. That is accomplished by centering shaft 162 with respect to the carriage 90 and positioning the trunnions 72, 74 equally spaced from the workpiece axis.
- the finishing tool such as grinding disk 20, is connected to the lower end of tool drive shaft 162 and is preferably partially enclosed by a shroud 170 held beneath the beam 150.
- a suitable exhaust manifold (not shown) may be connected to the shroud 170 to collect particulate material during a finishing operation.
- the platform generally 120, with motor 156 and grinding disk 20 are moved parallel to the carriage channels 92, 94 by a fluid cylinder 180 and reciprocable piston rod 182 connected between an angle 188 fastened between channels 92, 94 on the carriage generally 90 and an angle 190 on the platform depending plate 124.
- the cylinder is connectable to a suitable pressurized fluid supply (not shown - preferably pneumatic) and is operable to pull the platform 120 downwardly with a controllable force overcoming the bias of the compression springs 132, 134 and against the reaction of the workpiece (tube 10) against the flat grinding face 22 of grinding disk 20.
- the tool driving motor 156 is energized and pressurized fluid is introduced to the upper end of cylinder 180 to lower the platform generally 120 thereby extending the spinning grinding disk 20 downwardly until the abrasive surface 22 engages the end of tube 10.
- the tool driving motor 156 may be deenergized and the power cylinder 100 is again activated to extend its rod 102 thereby swinging the carriage 90 outwardly to the inoperative position moving the grinding disk 20 completely clear of the annular holder generally 30 and the tube 10 held therein. At that point the tube is extracted upwardly and a new workpiece inserted downwardly.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Grinding And Polishing Of Tertiary Curved Surfaces And Surfaces With Complex Shapes (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US68482491A | 1991-04-15 | 1991-04-15 | |
| US684824 | 1991-04-15 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0509665A2 true EP0509665A2 (de) | 1992-10-21 |
| EP0509665A3 EP0509665A3 (en) | 1993-03-03 |
Family
ID=24749731
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19920302772 Withdrawn EP0509665A3 (en) | 1991-04-15 | 1992-03-30 | Method and apparatus for grinding the end of a tubular workpiece |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP0509665A3 (de) |
| AU (1) | AU1102492A (de) |
| BR (1) | BR9201136A (de) |
| CA (1) | CA2061001C (de) |
| MX (1) | MX9201227A (de) |
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1077105A1 (de) * | 1999-06-25 | 2001-02-21 | Ernst Thielenhaus GmbH & Co. KG | Vorrichtung zum Feinschleifen von Stirnflächen an dünnwandigen und/oder kleinstückigen Serienteilen |
| RU2367557C1 (ru) * | 2008-05-30 | 2009-09-20 | Государственное образовательное учреждение высшего профессионального образования "Ульяновский государственный технический университет" | Способ плоского шлифования |
| CN104324924A (zh) * | 2014-11-13 | 2015-02-04 | 宁夏中远天宇科技有限公司 | 一种铁路货车制动软管生料带清除机的软管夹持器 |
| CN105798709A (zh) * | 2015-01-15 | 2016-07-27 | 日本碍子株式会社 | 端面研磨方法、以及端面研磨装置 |
| CN107309732A (zh) * | 2017-08-25 | 2017-11-03 | 文永林 | 一种天然气管道生产用管道边缘打磨装置 |
| CN108326515A (zh) * | 2018-01-31 | 2018-07-27 | 重庆聚伯雅科技有限公司 | 用于五金件的制作工艺 |
| CN109676455A (zh) * | 2019-01-21 | 2019-04-26 | 新乡辉簧弹簧有限公司 | 电机定子壳体端面打磨装置 |
| CN110860959A (zh) * | 2019-11-28 | 2020-03-06 | 贵州翰久士卫浴有限公司 | 管材自动加工方法 |
| CN114274001A (zh) * | 2021-12-21 | 2022-04-05 | 彭满艳 | 一种水利工程用水管端口打磨设备 |
| CN116237835A (zh) * | 2023-04-27 | 2023-06-09 | 大连瑞邦海洋科技有限公司 | 一种用于管件坡口打磨的装置 |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111716187B (zh) * | 2020-06-16 | 2022-02-25 | 福建和盛塑业有限公司 | 埋地电缆保护管用镀锌钢管焊接前对口处理方法 |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2998679A (en) * | 1959-09-04 | 1961-09-05 | Mattison Machine Works | Grinding machine |
| JPS57121451A (en) * | 1981-01-20 | 1982-07-28 | Takuma Co Ltd | Tube edge grinder |
-
1992
- 1992-02-11 CA CA 2061001 patent/CA2061001C/en not_active Expired - Lifetime
- 1992-02-17 AU AU11024/92A patent/AU1102492A/en not_active Abandoned
- 1992-03-19 MX MX9201227A patent/MX9201227A/es unknown
- 1992-03-30 EP EP19920302772 patent/EP0509665A3/en not_active Withdrawn
- 1992-03-31 BR BR929201136A patent/BR9201136A/pt not_active Application Discontinuation
Cited By (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1077105A1 (de) * | 1999-06-25 | 2001-02-21 | Ernst Thielenhaus GmbH & Co. KG | Vorrichtung zum Feinschleifen von Stirnflächen an dünnwandigen und/oder kleinstückigen Serienteilen |
| RU2367557C1 (ru) * | 2008-05-30 | 2009-09-20 | Государственное образовательное учреждение высшего профессионального образования "Ульяновский государственный технический университет" | Способ плоского шлифования |
| CN104324924A (zh) * | 2014-11-13 | 2015-02-04 | 宁夏中远天宇科技有限公司 | 一种铁路货车制动软管生料带清除机的软管夹持器 |
| CN105798709A (zh) * | 2015-01-15 | 2016-07-27 | 日本碍子株式会社 | 端面研磨方法、以及端面研磨装置 |
| EP3045267A3 (de) * | 2015-01-15 | 2016-08-10 | NGK Insulators, Ltd. | Endflächenschleifverfahren und endflächenschleifvorrichtung |
| US10046430B2 (en) | 2015-01-15 | 2018-08-14 | Ngk Insulators, Ltd. | End face grinding method and end face grinding device |
| CN107309732A (zh) * | 2017-08-25 | 2017-11-03 | 文永林 | 一种天然气管道生产用管道边缘打磨装置 |
| CN108326515A (zh) * | 2018-01-31 | 2018-07-27 | 重庆聚伯雅科技有限公司 | 用于五金件的制作工艺 |
| CN109676455A (zh) * | 2019-01-21 | 2019-04-26 | 新乡辉簧弹簧有限公司 | 电机定子壳体端面打磨装置 |
| CN110860959A (zh) * | 2019-11-28 | 2020-03-06 | 贵州翰久士卫浴有限公司 | 管材自动加工方法 |
| CN114274001A (zh) * | 2021-12-21 | 2022-04-05 | 彭满艳 | 一种水利工程用水管端口打磨设备 |
| CN116237835A (zh) * | 2023-04-27 | 2023-06-09 | 大连瑞邦海洋科技有限公司 | 一种用于管件坡口打磨的装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| CA2061001A1 (en) | 1992-10-16 |
| CA2061001C (en) | 1993-11-30 |
| EP0509665A3 (en) | 1993-03-03 |
| AU1102492A (en) | 1992-10-22 |
| MX9201227A (es) | 1992-10-01 |
| BR9201136A (pt) | 1992-12-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US6419443B2 (en) | Glass product machining apparatus | |
| CA2061001C (en) | Method of apparatus for grinding the end of a tubular workpiece | |
| CZ290918B6 (cs) | Zařízení pro brouąení vzorků materiálu | |
| EP0275028B1 (de) | Felge und Spindel für Reifen-Gleichförmigkeitsmaschinen | |
| US3224146A (en) | Apparatus for grinding drills | |
| US4068412A (en) | Grinding machine | |
| US4763515A (en) | Tire uniformity machine and method | |
| US4854082A (en) | Apparatus for grinding tooth replacement primary crown castings | |
| US5107703A (en) | Tire uniformity machine | |
| CN110142682B (zh) | 一种机械工件抛光设备 | |
| CN220944576U (zh) | 一种阀芯上下料定位机构 | |
| JPH07299512A (ja) | テーブルロール現地補修用ロール研磨装置 | |
| US3967415A (en) | Device for mounting and dismounting a grinding wheel assembly onto or from, respectively, the grinding spindle of a grinding machine | |
| CN110962044A (zh) | 金刚石磨盘定位装置 | |
| CN105014522A (zh) | 具有冷却液喷嘴的磨床 | |
| EP0263513A2 (de) | Bohrerschleifmaschine mit Bohrerhalter, versehen mit Spannfuttern zum Spannen des Bohrerschaftes und des Bohrerkörpers | |
| CN217097167U (zh) | 一种圆弧件往复抛光装置 | |
| CN117260529A (zh) | 一种阀芯研磨机 | |
| JPH03110138A (ja) | タイヤユニフォミティマシンにおけるリムチエンジャ装置 | |
| CN215616943U (zh) | 一种生产精密模具零件用精平面磨床 | |
| JPH079317A (ja) | 面取り研削された繊維強化プラスチック管の製造法および繊維強化プラスチック管の面取り研削装置 | |
| US6083086A (en) | Expanding device for grinding sleeves | |
| JP3261897B2 (ja) | ホーニングヘッドの成形加工方法及び成形加工装置 | |
| JP2695103B2 (ja) | 工具研削装置 | |
| CN211305756U (zh) | 一种对空心圆管件内孔打磨的装备 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): DE ES FR IT |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): DE ES FR IT |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19931004 |