EP0280857B1 - Dispositif de tri - Google Patents
Dispositif de tri Download PDFInfo
- Publication number
- EP0280857B1 EP0280857B1 EP88100738A EP88100738A EP0280857B1 EP 0280857 B1 EP0280857 B1 EP 0280857B1 EP 88100738 A EP88100738 A EP 88100738A EP 88100738 A EP88100738 A EP 88100738A EP 0280857 B1 EP0280857 B1 EP 0280857B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sorting device
- construction parts
- sensor
- rail
- screw
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000005259 measurement Methods 0.000 claims description 10
- 230000007547 defect Effects 0.000 claims description 9
- 238000009825 accumulation Methods 0.000 claims description 7
- 238000004806 packaging method and process Methods 0.000 claims description 3
- 230000000694 effects Effects 0.000 claims description 2
- 238000010276 construction Methods 0.000 claims 19
- 230000002950 deficient Effects 0.000 claims 6
- 230000000717 retained effect Effects 0.000 claims 1
- 101100298222 Caenorhabditis elegans pot-1 gene Proteins 0.000 description 3
- 239000000463 material Substances 0.000 description 3
- 230000003287 optical effect Effects 0.000 description 3
- 208000033985 Device component issue Diseases 0.000 description 2
- 238000006073 displacement reaction Methods 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 239000013590 bulk material Substances 0.000 description 1
- 238000001514 detection method Methods 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 230000001939 inductive effect Effects 0.000 description 1
- 238000004381 surface treatment Methods 0.000 description 1
- 230000001960 triggered effect Effects 0.000 description 1
- 238000002604 ultrasonography Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07C—POSTAL SORTING; SORTING INDIVIDUAL ARTICLES, OR BULK MATERIAL FIT TO BE SORTED PIECE-MEAL, e.g. BY PICKING
- B07C5/00—Sorting according to a characteristic or feature of the articles or material being sorted, e.g. by control effected by devices which detect or measure such characteristic or feature; Sorting by manually actuated devices, e.g. switches
- B07C5/04—Sorting according to size
- B07C5/08—Sorting according to size measured electrically or electronically
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07C—POSTAL SORTING; SORTING INDIVIDUAL ARTICLES, OR BULK MATERIAL FIT TO BE SORTED PIECE-MEAL, e.g. BY PICKING
- B07C5/00—Sorting according to a characteristic or feature of the articles or material being sorted, e.g. by control effected by devices which detect or measure such characteristic or feature; Sorting by manually actuated devices, e.g. switches
- B07C5/04—Sorting according to size
- B07C5/06—Sorting according to size measured mechanically
- B07C5/065—Sorting according to size measured mechanically with multiple measuring appliances adjusted according to different standards, for example length or thickness, which detect the shape of an object so that if it conforms to the standard set by the measuring appliance, it is removed from the conveyor, e.g. by means of a number of differently calibrated openings
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10S—TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10S209/00—Classifying, separating, and assorting solids
- Y10S209/929—Fastener sorter
Definitions
- the invention relates to a sorting device according to the type of the main claim.
- a sorting device according to US Pat. No. 3,650,397 is already known, in which the screws to be sorted are in a transparent tube on an optical sensor, e.g. B. be guided past photodiodes. With the aid of a mirror, a shadow of the screw to be assessed is projected onto the sensor and this image is compared with the nominal dimensions. If the screw has a defect on its illustrated contour, it is rejected on a switch.
- This sorting device has the disadvantage that only the projection shadow can be checked in a single plane for each measurement. Errors on the non-projected circumference, on the surface or inside (slot shape) cannot be detected. In addition, the measuring accuracy depends on the conveying speed at the measuring point and on the stable position of the screw in the pipe.
- the sorting device according to the invention with the characterizing features of the main claim has the advantage that the complete shape of the screws, both their shape and their dimensions, their surface quality and their internal shapes (slots, cracks) can be determined with great accuracy. Furthermore, the measurement result is independent of the conveyor speed of the conveyor. The measurement is not - as with optical measuring methods - affected by dirt. Temperature influences are also irrelevant. In addition, the sorting device is much cheaper than optical systems.
- the conveyor can consist, for example, of a simple rail with a liner conveyor. The reliability of the sorting device is considerably improved by the combination of mechanical and electrical measuring points.
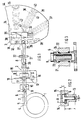
- Figure 1 shows a plan view of the entire sorting device.
- Figure 2 shows a cross section through the template 13 along the line II-II in Figure 1.
- Figure 3 shows a cross section through the shaft sensors 21 and 22.
- Figure 4 shows a measurement diagram of the shaft sensor.
- FIG. 5 shows a cross section through the head sensor 25.
- a screw spindle is shown in FIG.
- Figure 7 shows the control loop of the sorting device.
- the sorting device is divided into two main parts, a conveyor pot 1 and a linear section 2 with the devices for screw detection and rejection.
- a separating device 3 and one or more screw spindles or a packaging machine (not shown) can be connected to the linear section 2.
- the well-known conveyor pot 1 takes up the screws, nails, head bolts or the like as bulk material and brings them in a row hanging from a rail 4.
- the rail 4 has a slot 5 through which the shafts of the screws, but not the heads, can pass.
- the rail 4 continues seamlessly in the rail 6 belonging to the linear path 2 with a slot 7 corresponding to the slot 5.
- the rail 6 is fixedly connected to a linear conveyor 8, known per se, which, by means of vibration, exerts a linear conveying movement that is as constant as possible on the screws 9.
- the slot 7 widens to a hole 10 which is slightly smaller than the head diameter of the screw 9 to be tested and fall through the screwing with too small a head diameter into a collecting container 11 for unusable screws.
- the screw 9 is further conveyed onto an interchangeable slide 12 and comes to a template 13.
- the screw geometries conveyed are incorporated into the template 13 in relation to head diameter A, shaft diameter B, head height C and shaft length D ( Figure 2).
- the template 13 consists of two halves 14 and 15 so that they can be attached to the rail 6, e.g. by screws, not shown, which reach through the template halves 14 and 15 and are screwed into the narrow sides of the rail 6. If one of the required dimensions is exceeded, the screw material jams in the template 13.
- the interchangeable slide 12 consists of two short rail sections 16 and 17, which are guided on a rod 18 and can be inserted alternately into a gap in the rail 6. Below the interchangeable slide 12 there is a collecting container 19, into which screws of the dimensionally unstable screws removed from the interchangeable slide from the linear path 2 are due to the conveying effect also exerted on the rail sections 16 and 17 of the linear conveyor 8 fall into it.
- the shuttle valve 12 receives its release signal from a control device 50, which will be described later.
- a traffic jam sensor 20 is arranged above the rail 6 and can detect whether there are screws under it or not.
- the traffic jam sensor 20 can operate according to mechanical, inductive, capacitive, piezoelectric, ultrasound or the eddy current principle or according to other principles and emits its signal to the electrical or pneumatic control device 50 (FIG. 7).
- the shaft sensor 21 Downstream of the accumulation sensor 20 is the shaft sensor 21, 22, which is inserted into recesses in the lateral flanks of the rail 6 (FIG. 3).
- the shaft sensor consists of two parts 21, 22, in each of which a coil 23, 24 is arranged.
- the coils preferably work according to the eddy current principle, the mode of operation of which is described in more detail in our application P 37 06 574.2 (filed on the same day) and with which surface defects can also be easily recognized.
- plates can also be contained in the shaft sensor and the measurement can be carried out capacitively.
- the following dimensions can be monitored with the aid of the shaft sensor 21, 22: shaft diameter, shaft length, thread defects, material defects such as cracks or cavities, and surface defects, for example poor surface treatment.
- a measurement signal results, which is shown in FIG. 4.
- the time t is plotted on the right, the height of the measurement signal upwards.
- the first three screws are within the tolerance range T and are OK.
- the next four screws are faulty and generate a measurement signal that is too low. Since errors can be compensated for with this measuring method, e.g. shaft diameter too small / thread missing or shaft too long / blowholes
- Some criteria were previously checked mechanically through the hole 10 and the template 13 and defective screws were sorted out.
- the test criteria to be monitored by the shaft sensor 21, 22 are therefore reduced to: shaft diameter too small, shaft length too short, thread, material and surface defects.
- the reliability of the sorting device can be increased even further by arranging several pairs of coils along the screw shaft.
- the shaft sensor 21, 22 registers both a counting pulse Z (FIG. 4) with a running nunmer, which is triggered each time a screw is passed, and the height of the shaft signal. If the measurement signal voltage lies outside the permissible tolerance range T, an error signal is assigned to the counting pulse of this screw and the screw is further conveyed to the separating block 30.
- a head sensor 25 arranged there also registers counting pulses with a serial number. If there appears a screw with a number to which an error signal is assigned, it is assigned to the feed slide 38 for defective screws.
- the signals are expediently processed by a controller developed for this purpose.
- the head sensor 25 is attached at a defined constant distance K above the rail 6 or the receiving fork 27 (FIG. 5).
- the coil 26 arranged in the head sensor 25 also works according to the eddy current principle according to our application P 37 06 574.2.
- the head sensor 25 detects the following errors: head height too low (head height too high is checked by template 13), head diameter too large (head diameter too small is also checked by template 13), incorrect slot design or force application surfaces (e.g. slot instead of Torx, not existing slot) and surface defect and also registers the counting pulse described above.
- Faulty screws produce - similar to the shaft sensor (FIG. 4) - a measuring signal that is too large or too small. This immediately causes the feed slide 38 for faulty screws to be actuated.
- the rail 6 ends just before the head sensor 25 and continues seamlessly in the receiving cable 27 of the cross slide 28, which is guided in a guide link 29 of the separating block 30.
- the guide link 29 is arranged obliquely to the sliding direction of the separating slide 31, which conveys the tested screws at right angles to the rail 6 to the feed hole 32.
- the displacement of the separating slide 31 is accomplished by a work unit, not shown, which is connected to the push rod 33.
- the push rod is in turn firmly connected to the separating slide 31.
- the cross slide 28 withdraws from the screw due to the guide link 29 (to the right in FIG. 1) and releases the screw head, so that the screw can fall freely through the hole 32 into one of the metering slides 34 to 38 shown .
- a total of twelve metering slides can be attached to plate 44.
- the metering slides have housings 39 in which pistons 40 are guided.
- the piston rods 41 of the pistons 40 carry head pieces 42 with bores 43.
- inlet hoses not shown in FIG. 1, are connected, through which the individual screws are conveyed either for packaging or via the inlet hoses 61 to screw spindles 60 shown in FIG.
- sensors 63 are e.g. in the jaws 62 of the screw spindles 60 Vortex sensors are used, which either output the signal "screw in the pliers" or “no screw in the pliers” to the separating device 3.
- the control device 50 (FIG. 7) has the signal from the sensor 20 as the input variable and the acknowledgment of the feedback from the feed pot 1 about its operating state (on-off).
- the sensor signal passes through a signal processor 51 and a timing control circuit 51 with two Exits. One of the outputs either switches the feed pot on or off, the other actuates the change-over slide 12 in such a way that the rail section 16 or 17 currently in the linear section 2 is disengaged and the other rail section 17 or 16 is inserted into the gap in the linear section 2.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Sorting Of Articles (AREA)
- Sampling And Sample Adjustment (AREA)
Claims (20)
- Dispositif de tri pour pièces détachées de fixation avec têtes, en particulier des vis, avec un dispositif de transport constitué comme une piste linéaire (2), dispositif de tri caractérisé en ce que sur le dispositif de transport sont disposés plusieurs postes de mesure mécaniques et électriques (10, 13, 21, 22, 25), qui détectent les pièces dont les dimensions sont défectueuses, ainsi que des dispositifs d'éjection (10, 12, 3) associés aux postes respectifs de mesure, dispositifs d'éjection qui éliminent ces pièces défectueuses, les postes de mesure mécaniques (10, 13) étant placés avant les postes de mesure électriques (21, 22, 25).
- Dispositif de tri selon la revendication 1, caractérisé par un détecteur d'accumulation (20), qui peut détecter l'existence de pièces détachées de fixation sur la piste linéaire (2) et délivre des signaux correspondant à un dispositif de régulation (50).
- Dispositif de tri selon la revendication 2, caractérisé en ce que le détecteur d'accumulation (20) fonctionne selon le principe des courants de Foucault.
- Dispositif de tri selon l'une des revendications 2 et 3, caractérisé en ce que le dispositif de régulation (50) comporte un appareil de préparation des signaux (51) et un circuit de synchronisation (52) et deux sorties, une sortie pour le branchement du dispositif d'alimentation des vis, en particulier d'un pot d'alimentation (1) et une sortie pour actionner un dispositif d'éjection en particulier un poussoir alternatif (12).
- Dispositif de tri selon la revendication 4, caractérisé en ce que le dispositif de régulation (50) débranche le pot d'alimentation (1) quand le détecteur d'alimentation (20) détecte une accumulation.
- Dispositif de tri selon la revendication 4, caractérisé en ce que le dispositif de régulation (50) déclenche le poussoir alternatif (12) quand survient une accumulation.
- Dispositif de tri selon la revendication 4, caractérisé en ce que le dispositif de régulation (50) enclenche le pot d'alimentation (1) quand le détecteur d'accumulation est resté assez longtemps sans vis.
- Dispositif de tri selon l'une des revendications précédentes, caractérisé en ce que la piste linéaire (2) présente un rail (6) avec un convoyeur linéaire (8), qui actionne le convoiement des pièce détachées de fixation en direction du dispositif d'individualisation (3).
- Dispositif de tri selon lune des revendications précédentes, caractérisé en ce que l'un des postes mécaniques de mesure consiste en un trou (10) dans le rail (6) de la piste linéaire (2), qui est à peine plus petit que le diamètre de la tête des pièces détachées de fixation à contrôler, en particulier des vis (9) et à travers lequel les pièces détachées, qui ont une tête dont le diamètre est trop petit, tombent dans un récipient de recueil (11).
- Dispositif de tri selon l'une des revendications précédentes, caractérisé en ce qu'un poste de mesure mécanique suivant consiste en un gabarit (13) avec une ouverture pour les pièces détachées de fixation, qui est dimensionné de telle sorte que sont retenues les pièces détachées qui ont une tête trop haute, un diamètre de tête trop grand, un diamètre de tige trop grand, une tige trop longue ou une forme extérieure qui s'écarte autrement de la norme.
- Dispositif de tri selon la revendication 10, caractérisé en ce que l'on dispose sur la piste de transport directement avant le gabarit (13) comme dispositif d'éjection un poussoir alternatif (12), qui écarte de la piste linéaire (2) une pièce détachée bloquée devant le gabarit (13).
- Dispositif de tri selon l'une des revendications précédentes, caractérisé en ce que l'un des postes de mesure électriques, un détecteur de tige (21, 22), est disposé sur le rail (6) dans la zone de la tige des pièces détachées de fixation se trouvant sur le rail (6), en particulier des vis (9), qui délivre, dans le cas où les tiges n'ont pas la dimension convenable ou sont défectueuses, un autre signal de mesure que celui délivré dans le cas des pièces détachées sans problème.
- Dispositif de tri selon l'une des revendications précédentes, caractérisé en ce que l'on dispose un autre poste de mesure électrique et en fait un détecteur de tête (25) au-dessus du rail (6) et que celui-ci dans le cas de têtes de pièces détachées défectueuses délivre un signal pour éliminer celles-ci.
- Dispositif de tri selon la revendication 12 et/ou 13, caractérisé en ce que les détecteurs (21, 22 ou 25) fonctionnent selon le principe des courants de Foucault 11.
- Dispositif de tri selon l'une des revendications précédentes, caractérisé en ce qu à la fin du dispositif de tri est disposé un dispositif d'individualisation (3), qui sépare les pièces détachées de fixation dont les dimensions sont correctes de celles qui sont défectueuses et peuvent être raccordées aux dispositifs d'emballage ou aux broches à vis (60).
- Dispositif de tri selon l'une des revendications précédentes, caractérisé en ce que l'un des organes de recueil du dispositif d'individualisation (3), en particulier un poussoir (38) est activé lors de la détection de pièces détachées défectueuses par les détecteurs (21, 22 ou 25) et recueille ces pièces.
- Dispositif de tri selon l'une des revendications précédentes, caractérisé en ce que les détecteurs (21, 22 et 25) enregistrent en outre une impulsion de comptage.
- Dispositif de tri selon la revendication 17, caractérisé en ce que, lorsqu il survient des pièces détachées défectueuses sur le détecteur de tige (21, 22) un signal de défaut est associé à l'impulsion de comptage de ces pièces détachées.
- Dispositif de tri selon la revendication 18, caractérisé en ce qu'il est prévu une commande, qui enregistre les impulsions de comptage des détecteurs (21, 22 et 25) et actionne le poussoir d'éjection (38) pour pièces détachées défectueuses, quand survient sur le détecteur de têtes (25) une impulsion de comptage ave signal de défaut.
- Dispositif de tri selon l'une des revendications précédentes, caractérisé en ce que dans les mors (62) des broches à vis (60) sont disposés des détecteurs, qui quand il y a une vis délivrent un autre signal, que celui délivré quand aucune vis ne se trouve dans les mors (62).
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19873706575 DE3706575A1 (de) | 1987-02-28 | 1987-02-28 | Sortiereinrichtung |
| DE3706575 | 1987-02-28 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0280857A2 EP0280857A2 (fr) | 1988-09-07 |
| EP0280857A3 EP0280857A3 (en) | 1989-08-30 |
| EP0280857B1 true EP0280857B1 (fr) | 1993-11-18 |
Family
ID=6322043
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP88100738A Expired - Lifetime EP0280857B1 (fr) | 1987-02-28 | 1988-01-20 | Dispositif de tri |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US4905842A (fr) |
| EP (1) | EP0280857B1 (fr) |
| DE (2) | DE3706575A1 (fr) |
| ES (1) | ES2046993T3 (fr) |
Families Citing this family (28)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3827337A1 (de) * | 1988-08-12 | 1990-02-15 | Bosch Gmbh Robert | Sortiereinrichtung |
| DE4002992C2 (de) * | 1990-02-01 | 1994-12-08 | Horst Linnerbauer | Verfahren zum Vereinzeln und Ausrichten von Werkstücken und Bauteilen sowie zugehörige Zuführvorrichtung |
| US5165551A (en) * | 1990-03-30 | 1992-11-24 | Automation Associates, Inc. | Apparatus and method for detecting defects in an article |
| US5777246A (en) * | 1995-12-01 | 1998-07-07 | The Boeing Company | Fastener measurement system |
| US5823356A (en) * | 1996-04-25 | 1998-10-20 | Ajax Metal Processing, Inc. | Apparatus and method for insepcting threaded members |
| US6004215A (en) * | 1997-11-05 | 1999-12-21 | L & M Machinery & Manufacturing | Fastener forming machine |
| DE20015407U1 (de) * | 2000-09-06 | 2002-01-17 | Emhart Inc., Newark, Del. | Vereinzelungsvorrichtung |
| US6787724B2 (en) * | 2001-08-24 | 2004-09-07 | Attica Automation | Sorting machine |
| US20050174567A1 (en) * | 2004-02-09 | 2005-08-11 | Mectron Engineering Company | Crack detection system |
| US7416086B2 (en) * | 2004-05-03 | 2008-08-26 | Acument Intellectual Properties Llc | In-line sorter for fasteners |
| TWM269975U (en) * | 2004-05-21 | 2005-07-11 | Aerser Internat Co Ltd | Screw inspection machinery |
| DE102004030667B4 (de) * | 2004-06-24 | 2017-10-19 | Gassner Ges.M.B.H. | Sortiergerät |
| DE202004017425U1 (de) * | 2004-11-10 | 2005-01-13 | Böllhoff Verbindungstechnik GmbH | Mess- und Sortiervorrichtung |
| WO2008071204A1 (fr) * | 2006-12-12 | 2008-06-19 | Montanuniversität Leoben | Système et procédé pour l'analyse de défauts de pièces |
| US20080174107A1 (en) * | 2007-01-23 | 2008-07-24 | Burl Jordan | System and Method for Identifying Irrigation Fittings |
| US7491319B1 (en) * | 2008-03-17 | 2009-02-17 | Te Hung En Enterprise Co., Ltd. | Inspecting apparatus with eddy current inspection |
| US8204294B2 (en) * | 2009-11-25 | 2012-06-19 | Toyota Motor Engineering & Manufacturing North America, Inc. | Systems and methods for detecting defects in coatings utilizing color-based thermal mismatch |
| US8789446B1 (en) | 2011-06-28 | 2014-07-29 | Western Digital Technologies, Inc. | Screw feeding apparatus to deliver a screw from a vibrating rail to a screw guide tube |
| US9150360B1 (en) | 2013-05-16 | 2015-10-06 | Western Digital Technologies, Inc. | Mechanism to deliver fastener vertically |
| CN104215190A (zh) * | 2014-08-13 | 2014-12-17 | 常州精研科技有限公司 | 手机微小零部件的内螺纹检测装置 |
| CN104624521A (zh) * | 2015-03-02 | 2015-05-20 | 上海众源燃油分配器制造有限公司 | 一种螺母螺纹及裂缝自动检测设备 |
| US9731328B2 (en) | 2015-08-03 | 2017-08-15 | Linear Group Services, LLC | Inspection and sorting machine |
| CN106066362A (zh) * | 2016-05-24 | 2016-11-02 | 海盐正联检测技术有限公司 | 螺栓紧固件自动化硬度检测和筛选打包系统 |
| JP6705983B2 (ja) * | 2016-07-28 | 2020-06-03 | 青山 省司 | 頭部付き軸状部品の選別構造部 |
| DE102016124694B4 (de) * | 2016-12-16 | 2020-06-10 | Peter Müller | Fügeelemente-Bereitstellungsvorrichtung sowie zugehörige Robotervorrichtung |
| CN114460320B (zh) * | 2022-04-14 | 2022-06-21 | 深圳市帝迈生物技术有限公司 | 样本分析仪及其样本检测流程 |
| CN118954030B (zh) * | 2024-07-29 | 2026-01-02 | 中交一公局第三工程有限公司 | 一种盾构隧道连续与垂直皮带机相结合的智能出渣系统 |
| CN120861419B (zh) * | 2025-09-29 | 2025-12-09 | 联钢精密科技(中国)有限公司 | 一种具有防划伤功能的螺母检测分料装置 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1125272A (en) * | 1966-01-10 | 1968-08-28 | Continental Can Co | Improvements in sensing variations in the profiles of electrically conductive parts of objects |
| US3650397A (en) * | 1970-11-19 | 1972-03-21 | Sensors Inc | System for inspecting and classifying objects such as screws, bolts and the like while in motion |
Family Cites Families (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2464449A (en) * | 1949-03-15 | Johnston | ||
| US2310661A (en) * | 1940-05-14 | 1943-02-09 | Glenn L Martin Co | Sorting machine |
| US3091332A (en) * | 1958-09-25 | 1963-05-28 | Aluminium Lab Ltd | Inspecting or sorting apparatus |
| US3455446A (en) * | 1967-09-05 | 1969-07-15 | Burton S Seafood Inc | Apparatus and method for advancing objects to gauging slots |
| US3539006A (en) * | 1968-05-22 | 1970-11-10 | Lamson & Sessions Co | Method and apparatus for inspecting annular articles |
| FR2071351A5 (fr) * | 1969-12-24 | 1971-09-17 | Lamson Sessions Co | |
| US3709328A (en) * | 1970-08-12 | 1973-01-09 | Reich Maschf Gmbh Karl | Fastener sorting apparatus |
| US4174028A (en) * | 1974-06-13 | 1979-11-13 | Amerace Corporation | Method and apparatus for orienting and storing similar articles |
| US4002560A (en) * | 1975-07-24 | 1977-01-11 | Grantham Frederick W | Automatic article sorting apparatus |
| DE2609081C3 (de) * | 1976-03-05 | 1979-04-12 | Maschinenfabrik Lorenz Ag, 7505 Ettlingen | Vorrichtung zum Sortieren von Gegenständen |
| US4410078A (en) * | 1978-01-05 | 1983-10-18 | The Continental Group, Inc. | Article density sensing |
| US4341311A (en) * | 1980-08-25 | 1982-07-27 | Deere & Company | Method and apparatus for sorting rivets |
| US4454947A (en) * | 1981-12-07 | 1984-06-19 | Olin Corporation | Product inspection and ejection system |
| GB2111213A (en) * | 1981-12-09 | 1983-06-29 | Neuss Schraubenwerk | Method and apparatus for sorting screws |
| US4457622A (en) * | 1982-01-27 | 1984-07-03 | Nhk Spring Co., Ltd. | Screw inspection device |
| US4487321A (en) * | 1982-07-01 | 1984-12-11 | Diamond Automations, Inc. | Article coding and separating system |
| US4576286A (en) * | 1983-06-27 | 1986-03-18 | Cochlea Corporation | Parts sorting systems |
| US4602711A (en) * | 1984-06-15 | 1986-07-29 | Wullenwaber Robert W | Apparatus for feeding cylindrical workpieces to a workplace |
-
1987
- 1987-02-28 DE DE19873706575 patent/DE3706575A1/de not_active Withdrawn
-
1988
- 1988-01-12 US US07/143,445 patent/US4905842A/en not_active Expired - Fee Related
- 1988-01-20 EP EP88100738A patent/EP0280857B1/fr not_active Expired - Lifetime
- 1988-01-20 ES ES88100738T patent/ES2046993T3/es not_active Expired - Lifetime
- 1988-01-20 DE DE88100738T patent/DE3885629D1/de not_active Expired - Fee Related
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1125272A (en) * | 1966-01-10 | 1968-08-28 | Continental Can Co | Improvements in sensing variations in the profiles of electrically conductive parts of objects |
| US3650397A (en) * | 1970-11-19 | 1972-03-21 | Sensors Inc | System for inspecting and classifying objects such as screws, bolts and the like while in motion |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0280857A2 (fr) | 1988-09-07 |
| US4905842A (en) | 1990-03-06 |
| ES2046993T3 (es) | 1994-02-16 |
| DE3706575A1 (de) | 1988-09-08 |
| DE3885629D1 (de) | 1993-12-23 |
| EP0280857A3 (en) | 1989-08-30 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0280857A2 (fr) | Dispositif de tri | |
| DE69511586T2 (de) | Sortiersystem mit Querband | |
| DE3883681T2 (de) | Verfahren und Anordnung zum Vereinzeln von Gegenständen auf einem Fördersystem. | |
| EP0270133B1 (fr) | Dispositif d'alimentation de pièces | |
| DE3325125C1 (de) | Anordnung zur Markierung von Fehlstellen an schnell laufenden Materialbahnen | |
| DE2936573A1 (de) | Blattzaehlverfahren und -vorrichtung | |
| DE4302656C2 (de) | Verfahren und Vorrichtung zum Überprüfen der Funktionsfähigkeit von Inspektionseinrichtungen an Flascheninspektionsmaschinen | |
| DE602004004249T2 (de) | Verfahren zum detektieren und beseitigen fehlerhafter zigaretten | |
| EP3512788B1 (fr) | Procédé et dispositif de tri d'objets en forme de disque | |
| DE3611370C2 (fr) | ||
| DE1761466C3 (de) | Sackmaschine | |
| EP0180283A2 (fr) | Dispositif pour la lecture à leur passage d'objets ou de bacs de transport pourvus d'un porteur d'informations | |
| DE4312550C1 (de) | Vorrichtung zur Bewertung von sich fortbewegenden Objekten | |
| DE4019203A1 (de) | Verfahren und vorrichtung zum sortieren von altglas | |
| DE3730307C2 (de) | Zuführeinrichtung mit Vorratskammern | |
| DE3924274A1 (de) | Transporteinrichtung zum zufuehren und abtransportieren von vollen und leeren packungstraegern zu und von wenigstens einer spinnereimaschine | |
| DE4404912B4 (de) | Verfahren und Vorrichtung zum Überprüfen der genauen Positionierung des Filterpapiers von Zigaretten | |
| DE10039149C2 (de) | Vorrichtung zur schnellen lagegerechten Zuführung von Teilen | |
| EP0893516A1 (fr) | Procédé et appareil pour identifier des matières étrangères selon leur lieu de provenance dans des balles de fibres, en particulier balles de coton | |
| DE2520163A1 (de) | Verfahren zur automatisierung einer stabeisen-versandvorbereitungsstrasse und strasse zur durchfuehrung dieses verfahrens | |
| DE3508576C1 (de) | Vorrichtung zur Objektkontrolle mittels Objektvergleich | |
| DE3007540A1 (de) | Vorrichtung zum pruefen und aussortieren von fremdflaschen | |
| DE2837362C2 (de) | Einrichtung zum selbsttätigen Prüfen viereckiger Bleche längs eines Transportsystems | |
| GB1604842A (en) | Apparatus for determining a dimension of an article | |
| DE2410648C3 (de) | Verfahren zur Feststellung und zur Eliminierung von Zählfehlern |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): DE ES FR GB IT SE |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): DE ES FR GB IT SE |
|
| 17P | Request for examination filed |
Effective date: 19900206 |
|
| RAP3 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: ROBERT BOSCH GMBH |
|
| 17Q | First examination report despatched |
Effective date: 19920403 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT SE |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19931117 |
|
| ET | Fr: translation filed | ||
| REF | Corresponds to: |
Ref document number: 3885629 Country of ref document: DE Date of ref document: 19931223 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 19940117 Year of fee payment: 7 |
|
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2046993 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19950121 |
|
| EAL | Se: european patent in force in sweden |
Ref document number: 88100738.9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19971219 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19980120 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19980122 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19980320 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990120 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990121 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 19990301 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19990120 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19991103 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050120 |