WO2020145366A1 - 複合部材 - Google Patents
複合部材 Download PDFInfo
- Publication number
- WO2020145366A1 WO2020145366A1 PCT/JP2020/000541 JP2020000541W WO2020145366A1 WO 2020145366 A1 WO2020145366 A1 WO 2020145366A1 JP 2020000541 W JP2020000541 W JP 2020000541W WO 2020145366 A1 WO2020145366 A1 WO 2020145366A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- metal
- inorganic porous
- porous layer
- composite member
- layer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B18/00—Layered products essentially comprising ceramics, e.g. refractory products
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C24/00—Coating starting from inorganic powder
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B1/00—Layered products having a non-planar shape
- B32B1/08—Tubular products
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/02—Layer formed of wires, e.g. mesh
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/14—Layered products comprising a layer of metal next to a fibrous or filamentary layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/16—Layered products comprising a layer of metal next to a particulate layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/18—Layered products comprising a layer of metal comprising iron or steel
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B3/00—Layered products comprising a layer with external or internal discontinuities or unevennesses, or a layer of non-planar shape; Layered products comprising a layer having particular features of form
- B32B3/26—Layered products comprising a layer with external or internal discontinuities or unevennesses, or a layer of non-planar shape; Layered products comprising a layer having particular features of form characterised by a particular shape of the outline of the cross-section of a continuous layer; characterised by a layer with cavities or internal voids ; characterised by an apertured layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B7/00—Layered products characterised by the relation between layers; Layered products characterised by the relative orientation of features between layers, or by the relative values of a measurable parameter between layers, i.e. products comprising layers having different physical, chemical or physicochemical properties; Layered products characterised by the interconnection of layers
- B32B7/02—Physical, chemical or physicochemical properties
- B32B7/027—Thermal properties
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B9/00—Layered products comprising a layer of a particular substance not covered by groups B32B11/00 - B32B29/00
- B32B9/005—Layered products comprising a layer of a particular substance not covered by groups B32B11/00 - B32B29/00 comprising one layer of ceramic material, e.g. porcelain, ceramic tile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B9/00—Layered products comprising a layer of a particular substance not covered by groups B32B11/00 - B32B29/00
- B32B9/04—Layered products comprising a layer of a particular substance not covered by groups B32B11/00 - B32B29/00 comprising such particular substance as the main or only constituent of a layer, which is next to another layer of the same or of a different material
- B32B9/041—Layered products comprising a layer of a particular substance not covered by groups B32B11/00 - B32B29/00 comprising such particular substance as the main or only constituent of a layer, which is next to another layer of the same or of a different material of metal
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/01—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics
- C04B35/10—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics based on aluminium oxide
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B37/00—Joining burned ceramic articles with other burned ceramic articles or other articles by heating
- C04B37/02—Joining burned ceramic articles with other burned ceramic articles or other articles by heating with metallic articles
- C04B37/021—Joining burned ceramic articles with other burned ceramic articles or other articles by heating with metallic articles in a direct manner, e.g. direct copper bonding [DCB]
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
- C23C28/04—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D only coatings of inorganic non-metallic material
- C23C28/042—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D only coatings of inorganic non-metallic material including a refractory ceramic layer, e.g. refractory metal oxides, ZrO2, rare earth oxides
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F21/00—Constructions of heat-exchange apparatus characterised by the selection of particular materials
- F28F21/04—Constructions of heat-exchange apparatus characterised by the selection of particular materials of ceramic; of concrete; of natural stone
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F3/00—Plate-like or laminated elements; Assemblies of plate-like or laminated elements
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2250/00—Layers arrangement
- B32B2250/02—2 layers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
- B32B2255/02—Coating on the layer surface on fibrous or filamentary layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
- B32B2255/06—Coating on the layer surface on metal layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
- B32B2255/20—Inorganic coating
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
- B32B2255/20—Inorganic coating
- B32B2255/205—Metallic coating
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
- B32B2255/28—Multiple coating on one surface
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2262/00—Composition or structural features of fibres which form a fibrous or filamentary layer or are present as additives
- B32B2262/10—Inorganic fibres
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2264/00—Composition or properties of particles which form a particulate layer or are present as additives
- B32B2264/10—Inorganic particles
- B32B2264/102—Oxide or hydroxide
- B32B2264/1022—Titania
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2264/00—Composition or properties of particles which form a particulate layer or are present as additives
- B32B2264/10—Inorganic particles
- B32B2264/102—Oxide or hydroxide
- B32B2264/1023—Alumina
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2307/00—Properties of the layers or laminate
- B32B2307/30—Properties of the layers or laminate having particular thermal properties
- B32B2307/302—Conductive
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2307/00—Properties of the layers or laminate
- B32B2307/30—Properties of the layers or laminate having particular thermal properties
- B32B2307/304—Insulating
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2307/00—Properties of the layers or laminate
- B32B2307/70—Other properties
- B32B2307/724—Permeability to gases, adsorption
- B32B2307/7242—Non-permeable
- B32B2307/7244—Oxygen barrier
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2457/00—Electrical equipment
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/32—Metal oxides, mixed metal oxides, or oxide-forming salts thereof, e.g. carbonates, nitrates, (oxy)hydroxides, chlorides
- C04B2235/3231—Refractory metal oxides, their mixed metal oxides, or oxide-forming salts thereof
- C04B2235/3232—Titanium oxides or titanates, e.g. rutile or anatase
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/32—Metal oxides, mixed metal oxides, or oxide-forming salts thereof, e.g. carbonates, nitrates, (oxy)hydroxides, chlorides
- C04B2235/3231—Refractory metal oxides, their mixed metal oxides, or oxide-forming salts thereof
- C04B2235/3244—Zirconium oxides, zirconates, hafnium oxides, hafnates, or oxide-forming salts thereof
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/50—Constituents or additives of the starting mixture chosen for their shape or used because of their shape or their physical appearance
- C04B2235/52—Constituents or additives characterised by their shapes
- C04B2235/5208—Fibers
- C04B2235/5216—Inorganic
- C04B2235/522—Oxidic
- C04B2235/5224—Alumina or aluminates
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/50—Constituents or additives of the starting mixture chosen for their shape or used because of their shape or their physical appearance
- C04B2235/52—Constituents or additives characterised by their shapes
- C04B2235/5292—Flakes, platelets or plates
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/70—Aspects relating to sintered or melt-casted ceramic products
- C04B2235/74—Physical characteristics
- C04B2235/78—Grain sizes and shapes, product microstructures, e.g. acicular grains, equiaxed grains, platelet-structures
- C04B2235/785—Submicron sized grains, i.e. from 0,1 to 1 micron
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/70—Aspects relating to sintered or melt-casted ceramic products
- C04B2235/74—Physical characteristics
- C04B2235/78—Grain sizes and shapes, product microstructures, e.g. acicular grains, equiaxed grains, platelet-structures
- C04B2235/786—Micrometer sized grains, i.e. from 1 to 100 micron
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2237/00—Aspects relating to ceramic laminates or to joining of ceramic articles with other articles by heating
- C04B2237/30—Composition of layers of ceramic laminates or of ceramic or metallic articles to be joined by heating, e.g. Si substrates
- C04B2237/32—Ceramic
- C04B2237/34—Oxidic
- C04B2237/343—Alumina or aluminates
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/622—Forming processes; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/62227—Forming processes; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products obtaining fibres
- C04B35/62231—Forming processes; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products obtaining fibres based on oxide ceramics
- C04B35/62259—Fibres based on titanium oxide
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/71—Ceramic products containing macroscopic reinforcing agents
- C04B35/78—Ceramic products containing macroscopic reinforcing agents containing non-metallic materials
- C04B35/80—Fibres, filaments, whiskers, platelets, or the like
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F13/00—Arrangements for modifying heat-transfer, e.g. increasing, decreasing
- F28F2013/001—Particular heat conductive materials, e.g. superconductive elements
Definitions
- This specification discloses the technique regarding a composite member.
- an inorganic protective layer is provided on the surface of the metal to form a composite member of the metal and the inorganic material.
- Patent Document 1 Japanese Unexamined Patent Application Publication No. 2018-33245 (hereinafter referred to as Patent Document 1) mainly coats a metal surface with an inorganic protective layer in order to impart heat resistance to automobile engine parts (metal).
- Patent Document 1 in order to prevent the inorganic protective layer from peeling from the metal due to the difference in thermal expansion coefficient between the metal and the inorganic protective layer, an amorphous inorganic material layer (specifically, borosilicate) is formed on the metal surface. Glass), and non-oxide ceramics (specifically, silicon carbide) is formed on the surface of the amorphous inorganic material layer.
- Patent Document 1 a relaxation layer (borosilicate glass) is provided between the metal and the functional layer (silicon carbide) that functions as a protective layer to reduce the difference in thermal expansion coefficient between the two. There is.
- the adhesion between the metal and the functional layer is improved by providing an amorphous relaxation layer.
- Patent Document 1 an amorphous relaxation layer is provided between the metal and the functional layer. Therefore, when forming the functional layer, it is necessary to form the functional layer at a temperature not exceeding the softening point of the relaxation layer. In other words, the material that can be used as the functional layer is limited to the material that can be formed into a film without exceeding the softening point of the relaxation layer. Therefore, the composite member of Patent Document 1 has low flexibility of materials (relaxation layer, functional layer) that can be used. Further, since the composite member of Patent Document 1 uses the amorphous relaxation layer, the improvement in heat resistance is limited. Therefore, continuous improvement is required in the field of composite materials. The present specification aims to provide a novel composite member that has never existed before.
- the composite material disclosed in the present specification may have an inorganic porous layer provided on the surface of a metal.
- the inorganic porous layer may include ceramic fibers.
- the inorganic porous layer may be composed of 15% by mass or more of alumina component and 45% by mass or more of titania component.
- the inorganic porous layer contains ceramic fibers. Therefore, the inorganic porous layer itself can absorb the influence of the difference in thermal expansion coefficient between the metal and the inorganic porous layer.
- a relaxation layer amorphous layer or the like is provided between the metal and the inorganic porous layer. Without providing, it is possible to prevent the inorganic porous layer from peeling from the metal.
- an inorganic “porous layer” is provided on the metal surface.
- Porous bodies typically have a high ability to "break" the environment inside and outside through the porous body. Therefore, the composite member suppresses the influence of the external environment on the metal or suppresses the influence of the metal on the external environment, and realizes high heat insulation and high sound insulation (sound absorption). be able to.
- the inorganic porous layer can suppress contact of substances in the external environment (for example, foreign matter, moisture, etc.) such as adsorptivity and hygroscopicity with the metal.
- the composite member may utilize an inorganic porous layer to support a catalyst or the like on the metal surface.
- the term "porous” as used herein means that the porosity (porosity) of the inorganic porous layer is 45% by volume or more.
- the inorganic porous layer contains the ceramic fiber, the strength (mechanical strength) of the inorganic porous layer itself is prevented from being lowered. Further, since the inorganic porous layer is composed of 15% by mass or more of alumina component and 45% by mass or more of titania component, the inorganic porous layer itself has a high melting point, and the external environment of the composite member becomes high temperature. Can also maintain its shape.
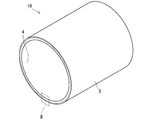
- An example (perspective view) of the composite member of the first embodiment is shown.
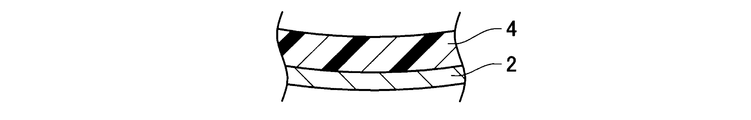
- the partial enlarged view of the composite member of 1st Example is shown.
- the cross-sectional view of the composite material of 1st Example is shown.
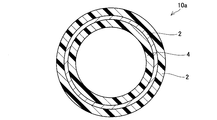
- the modification (cross section) of the composite material of 1st Example is shown.
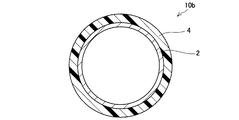
- the modification (cross section) of the composite material of 1st Example is shown.
- the modification (cross section) of the composite material of 1st Example is shown.
- An example (perspective view) of the composite member of the second embodiment is shown.
- An example (perspective view) of the composite member of the third embodiment is shown.
- An example (perspective view) of the composite member of the fourth embodiment is shown.
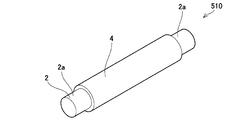
- An example (perspective view) of the composite member of the fifth embodiment is shown.
- An example (perspective view) of the composite member of the sixth embodiment is shown.
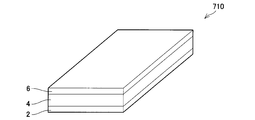
- An example (perspective view) of the composite member of the seventh embodiment is shown.
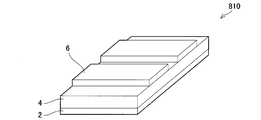
- An example (perspective view) of the composite member of the eighth embodiment is shown.
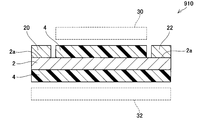
- the usage example (cross-sectional view) of a composite member is shown.
- the result of an experimental example is shown.
- plate-like ceramic particles may be included in the inorganic porous layer.
- the plate-shaped ceramic particles By using the plate-shaped ceramic particles, a part of the ceramic fibers can be replaced with the plate-shaped ceramic particles.
- the length (size in the longitudinal direction) of the plate-shaped ceramic particles is shorter than the length of the ceramic fibers. Therefore, by using the plate-like ceramic particles, the heat transfer path in the inorganic porous layer is divided, and heat transfer in the inorganic porous layer does not easily occur. As a result, the heat insulating performance of the inorganic porous layer is further improved.
- the “plate-like ceramic particles” mean ceramic particles having an aspect ratio of 5 or more and a longitudinal size of 5 ⁇ m or more and 50 ⁇ m or less.
- the inorganic porous layer may include granular particles of 0.1 ⁇ m or more and 10 ⁇ m or less.
- the ceramic fibers are bonded to each other through the granular particles to obtain a high-strength inorganic porous layer.
- the thickness of the inorganic porous layer may be 1 mm or more.
- the above-mentioned functions heat insulation, sound insulation, adsorption, hygroscopicity, etc.
- the inorganic porous layer of the composite member contains the ceramic fiber, the inorganic porous layer having a thickness of 1 mm or more can be realized.
- the inorganic porous layer can be formed to 1 mm or more.
- the inorganic porous layer shrinks in the process of molding and cracks or the like occur. Therefore, when the inorganic porous layer does not contain ceramic fibers, the inorganic porous layer It is difficult to form a thick layer having a thickness of 1 mm or more.
- an inorganic porous layer is provided on the surface of a metal. Moreover, the inorganic porous layer contains ceramic fibers.
- the inorganic porous layer is composed of 15% by mass or more and 55% by mass or less of the alumina (Al 2 O 3 ) component and 45% by mass or more and 85% by mass or less of the titania (TiO 2 ) component.
- the alumina component contained in the inorganic porous layer may be 25 mass% or more, 30 mass% or more, and 40 mass% or more.
- the composite member disclosed in this specification can be suitably used, for example, in a high temperature environment.
- the composite member can be preferably used as a member that constitutes an exhaust system of an automobile such as an exhaust manifold and an exhaust pipe.
- the composite member disclosed in the present specification can be suitably used, for example, as a heat conduction member that transfers heat generated by a heat source to a component (for example, a heat dissipation plate) existing at a position away from the heat source.
- the composite member may be arranged between a plurality of devices, and it can be suitably used as a partition plate that prevents heat generated from one device from being applied to the other device.
- the inorganic porous layer may coat the metal surface to protect the metal from the external environment.
- the “external environment” means the space on the opposite side of the metal through the inorganic porous layer. That is, when the composite material is a member forming the exhaust system of an automobile as described above, the "external environment” corresponds to the internal space of the exhaust manifold, the exhaust pipe, or the like.
- the inorganic porous layer may coat the metal surface to protect (insulate) the components present in the external environment of the composite member from the heat of the metal.
- the inorganic porous layer may cover both surfaces of two metals (for example, metal plates) facing each other with a gap.
- metal plates may be bonded to both surfaces of one inorganic porous layer. It is possible to prevent heat generated from the first device arranged on the first metal plate side from being applied to the second device arranged on the second metal plate side, and by the first metal plate, the first device The generated heat can be dissipated.
- the composite member suppresses the influence of heat by the metal and the external environment due to the inorganic porous layer.
- the inorganic porous layer separates spaces in which a plurality of devices are arranged, and suppresses the separated spaces from exerting influence of heat. Therefore, it is preferable that the metal and the inorganic porous layer have a large difference in thermal conductivity.
- the thermal conductivity of the metal may be 100 times or more the thermal conductivity of the inorganic porous layer.
- the thermal conductivity of the metal may be 150 times or more the thermal conductivity of the inorganic porous layer, 200 times or more the thermal conductivity of the inorganic porous layer, and the thermal conductivity of the inorganic porous layer.
- the thermal conductivity of the inorganic porous layer may be 250 times or more and 300 times or more of the thermal conductivity of the inorganic porous layer.
- the thermal conductivity of the metal may be 10 W/mK or more and 400 W/mK or less.
- the thermal conductivity of the metal may be 25 W/mK or higher, 50 W/mK or higher, 100 W/mK or higher, 150 W/mK or higher, 200 W/mK or higher. May be present, may be 250 W/mK or more, may be 300 W/mK or more, and may be 380 W/mK or more. Further, the thermal conductivity of the metal may be 350 W/mK or less, 300 W/mK or less, 250 W/mK or less, 200 W/mK or less, 150 W/mK or less. It may be.
- the thermal conductivity of the inorganic porous layer may be 0.05 W/mK or more and 3 W/mK or less.
- the thermal conductivity of the inorganic porous layer may be 0.1 W/mK or higher, 0.2 W/mK or higher, 0.3 W/mK or higher, 0.5 W/mK. Or more, 0.7 W/mK or more, 1 W/mK or more, 1.5 W/mK or more, and 2 W/mK or more.
- the thermal conductivity of the inorganic porous layer may be 2.5 W/mK or less, 2.0 W/mK or less, 1.5 W/mK or less, and 1 W/mK or less. It may be 0.5 W/mK or less, may be 0.3 W/mK or less, and may be 0.25 W/mK or less.
- the shape of the metal is not particularly limited, but may be tubular (cylindrical), linear (wire-shaped), or plate-shaped (sheet-shaped).
- the inorganic porous layer may coat the inner peripheral surface and/or the outer peripheral surface of the tubular metal.
- the linear metal is typically a solid structure. Therefore, in the case of a linear metal, the inorganic porous layer may cover the outer peripheral surface of the linear metal.
- the inorganic porous layer may cover the entire exposed surface of the plate-shaped metal or may cover the surface (front surface and/or back surface) of the end portion in the thickness direction. However, the surface (side surface) of the width direction end may be covered, or the surface of the length direction end may be covered.
- the inorganic porous layer covers both the front surface of the first plate-shaped metal (first metal plate) and the back surface of the second plate-shaped metal (second metal plate). Good.
- the inorganic porous layer may cover the entire metal surface, or may cover a part of the metal surface.
- the inorganic porous layer may cover a portion of the metal excluding the end portions (one end or both ends).
- the inorganic porous layer covers the inner and outer peripheral surfaces of the tubular metal, the inner peripheral surface is covered with the inorganic porous layer from one end to the other end (that is, the entire surface is covered), and the outer peripheral surface is the end. Areas covered with the inorganic porous layer may be different on the inner peripheral surface and the outer peripheral surface, for example, the portions other than the portions are covered.
- the inorganic porous layer covers the plate-shaped metal (for example, the surface of the end in the thickness direction: front and back surfaces)
- the inorganic porous layer is a part of the front and back surface (for example, one or both ends in the longitudinal direction).
- the part other than the part may be covered.
- the inorganic porous layer may cover the entire back surface, and cover the front surface, for example, a portion excluding both ends, and the range covered by the front and back surfaces may be different.
- the inorganic porous layer may be made of a uniform material in the thickness direction (the range from the surface in contact with the metal surface to the surface exposed to the external environment). That is, the inorganic porous layer may be a single layer. Further, the inorganic porous layer may be composed of a plurality of layers having different compositions in the thickness direction. That is, the inorganic porous layer may have a multilayer structure in which a plurality of layers are laminated. Alternatively, the inorganic porous layer may have a graded structure in which the composition gradually changes in the thickness direction. When the inorganic porous layer is a single layer, the production of the composite member (step of molding the inorganic porous layer on the metal surface) can be easily performed.
- the inorganic porous layer has a multilayer structure or a gradient structure
- the characteristics of the inorganic porous layer can be changed in the thickness direction.
- the structure of the inorganic porous layer (single layer, multilayer, inclined structure) can be appropriately selected according to the purpose of use of the composite member.
- the porosity of the inorganic porous layer may be 45% by volume or more and 90% by volume or less.
- the function of being porous such as heat insulating property, sound insulating property, adsorptive property, and hygroscopic property can be sufficiently exhibited.
- the catalyst can be sufficiently supported by utilizing the voids in the inorganic porous layer.
- the porosity is 90% by volume or less, sufficient strength can be secured.
- the porosity of the inorganic porous layer may be 55% by volume or more, 60% by volume or more, and may be 65% by volume or more.
- the porosity of the inorganic porous layer may be 85% by volume or less, 80% by volume or less, 70% by volume or less, 65% by volume or less, 60% by volume. It may be the following.
- the porosity of the inorganic porous layer may be 45% by volume or more and 90% by volume or less as a whole, and the porosities may be different in the thickness direction. .. In this case, a portion having a porosity of less than 45% by volume or a portion having a porosity of more than 90% by volume may be partially present.
- the thickness of the inorganic porous layer may be 1 mm or more, depending on the purpose of use (required performance).
- the functions of being porous such as heat insulating property, sound insulating property, adsorptive property and hygroscopic property, can be sufficiently exhibited.
- the thickness of the inorganic porous layer may be 30 mm or less, 20 mm or less, 15 mm or less, 100 mm or less, or 5 mm or less.
- the inorganic porous layer is composed of at least one material selected from ceramic particles (granular particles), plate-like ceramic particles, and ceramic fibers.
- the ceramic particles, plate-like ceramic particles and ceramic fibers may contain alumina and/or titania as a constituent component.
- the ceramic particles, the plate-shaped ceramic particles, and the ceramic fibers may be formed of alumina and/or titania. That is, the inorganic porous layer only needs to contain 15% by mass or more of an alumina component and 45% by mass or more of a titania component in the entire constituent material (constituent substance).
- the inorganic porous layer contains at least ceramic fibers, though the constituent components are optional (may or may not include the alumina component and the titania component).
- the ceramic particles may be used as a joining material for joining the aggregates forming the skeleton of the inorganic porous layer such as plate-like ceramic particles and ceramic fibers.
- the ceramic particles may be granular particles of 0.1 ⁇ m or more and 10 ⁇ m or less. It should be noted that the ceramic particles may have a large particle size due to sintering or the like in the manufacturing process (for example, a firing process). That is, as a raw material for producing the inorganic porous layer, the ceramic particles may be granular particles of 0.1 ⁇ m or more and 10 ⁇ m or less (average particle size before firing). The ceramic particles may be 0.5 ⁇ m or more and 5 ⁇ m or less.
- a metal oxide may be used as a material for the ceramic particles.
- the inorganic porous layer can be suitably applied as a protective layer for parts (exhaust manifold, etc.) of an automobile exhaust system, for example.
- the plate-shaped ceramics can function as an aggregate and a reinforcing material in the inorganic porous layer. That is, the plate-like ceramics improve the strength of the inorganic porous layer, like the ceramic fibers, and further suppress the shrinkage of the inorganic porous layer in the manufacturing process.
- the plate-shaped ceramic particles By using the plate-shaped ceramic particles, the heat transfer path in the inorganic porous layer can be divided. Therefore, when the composite member is used in a high temperature environment (when the inorganic porous layer is used for the purpose of insulating the metal), the heat insulating property can be improved as compared with the case where only the ceramic fiber is used as the aggregate. ..
- the plate-shaped ceramic particles may have a rectangular plate shape or a needle shape, and may have a longitudinal size of 5 ⁇ m or more and 100 ⁇ m or less.
- the size in the longitudinal direction is 5 ⁇ m or more, excessive sintering of ceramic particles can be suppressed.
- the size in the longitudinal direction is 100 ⁇ m or less, the effect of dividing the heat transfer path in the inorganic porous layer is obtained as described above, and it can be suitably applied to a composite member used in a high temperature environment.
- the plate-like ceramic particles may have an aspect ratio of 5 or more and 100 or less.
- the aspect ratio is 5 or more, it is possible to excellently suppress the sintering of the ceramic particles, and when the aspect ratio is 100 or less, the strength reduction of the plate-shaped ceramic particles themselves is suppressed.
- the material for the plate-shaped ceramic particles in addition to the metal oxide used as the material for the ceramic particles, talc (Mg 3 Si 4 O 10 (OH) 2 ), minerals such as mica, kaolin, clay, glass, etc. Can also be used.
- the ceramic fiber can function as an aggregate and a reinforcing material in the inorganic porous layer. That is, the ceramic fibers improve the strength of the inorganic porous layer and further suppress the shrinkage of the inorganic porous layer in the manufacturing process.
- the length of the ceramic fiber may be 50 ⁇ m or more and 200 ⁇ m or less. Further, the diameter (average diameter) of the ceramic fibers may be 1 to 20 ⁇ m.
- the volume ratio of the ceramic fibers in the inorganic porous layer (the volume ratio of the ceramic fibers in the material forming the inorganic porous layer) may be 5% by volume or more and 25% by volume or less.
- the ceramic fiber By containing 5% by volume or more of the ceramic fiber, it is possible to sufficiently suppress the shrinkage of the ceramic particles in the inorganic porous layer in the manufacturing process (firing step) of the inorganic porous layer. Further, by setting the volume ratio of the ceramic fibers to be 25% by volume or less, the heat transfer path in the inorganic porous layer can be divided, and it can be suitably applied to a composite member used in a high temperature environment.
- the material of the ceramic fiber the same material as the material of the plate-like ceramic particles described above can be used.
- the content of the aggregate and the reinforcing material (ceramic fiber, plate-like ceramic particles, etc., hereinafter simply referred to as aggregate) in the inorganic porous layer may be 15% by mass or more and 55% by mass or less.
- the content of the aggregate in the inorganic porous layer is 15% by mass or more, the shrinkage of the inorganic porous layer in the firing step can be sufficiently suppressed.
- the content ratio of the aggregate in the inorganic porous layer is 55% by mass or less, the aggregate is favorably bonded to each other by the ceramic particles.
- the content of the aggregate in the inorganic porous layer may be 20% by mass or more, 30% by mass or more, 50% by mass or more, and 53% by mass or more.
- the content of the aggregate in the inorganic porous layer may be 53 mass% or less, 50 mass% or less, 30 mass% or less, and even 20 mass% or less. Good.
- both the ceramic fibers and the plate-like ceramic particles can function as an aggregate and a reinforcing material in the inorganic porous layer.
- the content of ceramic fibers in the layer may be at least 5% by weight or more.
- the content of the ceramic fibers may be 10% by mass or more, 20% by mass or more, 30% by mass or more, and 40% by mass or more.
- the content of the ceramic fibers may be 50% by mass or less, 40% by mass or less, 30% by mass or less, 20% by mass or less, and 10% by mass or less. It may be.
- the ratio (weight ratio) of the plate-like ceramic particles in the whole aggregate may be 70% or less. That is, in terms of mass ratio, at least 30% or more of the aggregate may be ceramic fibers.
- the ratio (weight ratio) of the plate-shaped ceramic particles to the whole aggregate may be 67% or less, 64% or less, 63% or less, 60% or less, 50 It may be less than or equal to %.
- the plate-shaped ceramic particles are not always necessary as an aggregate. Further, the ratio of the plate-shaped ceramic particles to the entire aggregate may be 40% or more, 50% or more, 60% or more, 62% or more, 63% or more. And may be 65% or more.
- the content of the plate-shaped ceramic particles in the inorganic porous layer may be 5% by mass or more, 10% by mass or more, 20% by mass or more, 30% by mass. It may be above, and may be 33 mass% or more.
- the content of the plate-shaped ceramic particles may be 35% by mass or less, 33% by mass or less, 30% by mass or less, 20% by mass or less, and 10% by mass. It may be the following.
- SiO 2 contained in the inorganic porous layer may be 25 mass% or less. Formation of an amorphous layer in the inorganic porous layer is suppressed, and heat resistance (durability) of the inorganic porous layer is improved.
- a raw material obtained by mixing a binder, a pore-forming material, and a solvent may be used.
- An inorganic binder may be used as the binder.
- the inorganic binder include alumina sol, silica sol, titania sol, zirconia sol and the like. These inorganic binders can improve the strength of the inorganic porous layer after firing.
- the pore-forming material polymer-based pore-forming material, carbon-based powder or the like may be used. Specific examples thereof include acrylic resin, melamine resin, polyethylene particles, polystyrene particles, carbon black powder, and graphite powder.
- the pore-forming material may have various shapes depending on the purpose, and may have, for example, a spherical shape, a plate shape, or a fibrous shape.
- the porosity and pore size of the inorganic porous layer can be adjusted by selecting the addition amount, size and shape of the pore-forming material. Any solvent can be used as long as it can adjust the viscosity of the raw material without affecting other raw materials, and for example, water, ethanol, isopropyl alcohol (IPA) or the like can be used.
- IPA isopropyl alcohol
- the above-mentioned inorganic binder is also a constituent material of the inorganic porous layer. Therefore, when using alumina sol, titania sol or the like when forming the inorganic porous layer, the inorganic porous layer contains 15% by mass or more of the alumina component and 45% by mass or more of the titania component in the entire constituent material including the inorganic binder. It only needs to be included.
- the composition and raw material of the inorganic porous layer are adjusted according to the type of metal to be protected.
- the metal stainless steel such as SUS430, SUS429, SUS444, iron, copper, hastelloy, inconel, kovar, nickel alloy and the like can be used.
- the composition and raw material of the inorganic porous layer may be adjusted according to the thermal expansion coefficient of the metal used. Specifically, when the thermal expansion coefficient of the inorganic porous layer is ⁇ 1 and the thermal expansion coefficient of the metal is ⁇ 2, it may be adjusted so as to satisfy the following formula 1.
- the thermal expansion coefficient ⁇ 1 is preferably 6 ⁇ 10 ⁇ 6 /K ⁇ 1 ⁇ 14 ⁇ 10 ⁇ 6 /K, more preferably the thermal expansion coefficient ⁇ 1 is 6 ⁇ 10 ⁇ 6 /
- the composition and raw materials of the inorganic porous layer may be adjusted so that K ⁇ 1 ⁇ 11 ⁇ 10 ⁇ 6 /K.
- the thermal expansion coefficient ⁇ 1 is more preferably 8.5 ⁇ 10 ⁇ 6 /K ⁇ 1 ⁇ 20 ⁇ 10 ⁇ 6 /K, and more preferably the thermal expansion coefficient ⁇ 1 is 8.5 ⁇ .
- the composition and raw materials of the inorganic porous layer may be adjusted so that 10 ⁇ 6 /K ⁇ 1 ⁇ 18 ⁇ 10 ⁇ 6 /K.
- the value of “ ⁇ 1/ ⁇ 2” may be 0.55 or more, 0.6 or more, 0.65 or more, 0.75 or more, 0.8 It may be more than.
- the value of “ ⁇ 1/ ⁇ 2” may be 1.15 or less, 1.1 or less, 1.05 or less, or 1.0 or less.
- the above-mentioned raw material may be applied to the metal surface (in the case of tubular metal, the inside of the tube), and the inorganic porous layer may be formed on the metal surface after drying and firing.
- a method for applying the raw material dip coating, spin coating, spray coating, slit die coating, thermal spraying, aerosol deposition (AD) method, printing, brush coating, iron coating, mold cast molding or the like can be used.
- AD aerosol deposition
- coating of the raw material and drying of the raw material are repeated multiple times to adjust the target thickness or the multilayer structure. You may.
- the above coating method can also be applied as a coating method for forming a coating layer described later.
- a coating layer may be provided on the surface of the inorganic porous layer opposite to the surface provided with the metal. That is, the inorganic porous layer may be sandwiched between the metal and the coating layer.
- the coating layer may be provided on the entire surface of the inorganic porous layer (the surface opposite to the surface on which the metal is provided) or may be provided on a part of the surface of the inorganic porous layer. May be.
- the inorganic porous layer can be protected (reinforced) by providing the coating layer.
- the material of the coating layer may be porous or dense ceramics.
- porous ceramics used in the coating layer include zirconia (ZrO 2 ), partially stabilized zirconia, and stabilized zirconia.
- yttria-stabilized zirconia (ZrO 2 —Y 2 O 3 :YSZ) a metal oxide obtained by adding Gd 2 O 3 , Yb 2 O 3 , Er 2 O 3 or the like to YSZ, ZrO 2 —HfO 2 —Y 2 O 3 , ZrO 2 --Y 2 O 3 --La 2 O 3 , ZrO 2 --HfO 2 --Y 2 O 3 --La 2 O 3 , HfO 2 --Y 2 O 3 , CeO 2 --Y 2 O 3 , Gd 2 Zr 2 O 7 , Sm 2 Zr 2 O 7 , LaMnAl 11 O 19 , YTa 3 O 9 , Y 0.7 La 0.3 Ta 3 O 9 , Y 1.08 Ta 2.
- Examples of dense ceramics used in the coating layer include alumina, silica, zirconia, and the like. Further, by removing the ceramic fibers from the above-mentioned constituent material of the inorganic porous layer, a low porosity (denseness) is obtained, and therefore, it may be used as a coating layer.
- porous or dense ceramics as the coating layer, it is possible to reinforce the inorganic porous layer and prevent the inorganic porous layer from peeling off from the surface of the metal.
- a dense ceramic for example, high temperature gas can be prevented from passing through the inorganic porous layer, or high temperature gas can be prevented from staying in the inorganic porous layer. As a result, the effect of suppressing the heat of the high temperature gas from being transferred to the metal can be expected. Further, by using the dense ceramics as the coating layer, the effect of electrically insulating the metal from the external environment is improved.
- the material of the coating layer may be porous or dense glass.
- the use of porous or dense glass as the coating layer also reinforces the inorganic porous layer and prevents the inorganic porous layer from peeling off from the surface of the metal.
- the material of the coating layer may be a metal (a component separate from the metal protected by the inorganic porous layer).
- the composite member 10 will be described with reference to FIGS. 1 to 3.
- the composite member 10 includes the porous protective layer 4 on the inner surface of a tubular metal (metal tube) 2 made of SUS430.
- the porous protective layer 4 is an example of an inorganic porous layer.
- the porous protective layer 4 is bonded to the inner surface of the metal 2 (see FIGS. 1 and 2).
- the composite member 10 was manufactured by immersing the metal 2 in the raw material slurry with the outer surface of the metal 2 masked, followed by drying and firing.
- the raw material slurry includes alumina fibers (average fiber length 140 ⁇ m), plate-like alumina particles (average particle size 6 ⁇ m), titania particles (average particle size 0.25 ⁇ m), and alumina sol (alumina amount 1.1% by mass). Acrylic resin (average particle diameter 8 ⁇ m) and ethanol were mixed to prepare. The raw material slurry was adjusted to have a viscosity of 2000 mPa ⁇ s.
- the metal 2 was immersed in the raw material slurry to apply the raw material on the inner surface of the metal 2, the metal 2 was put into a dryer and dried at 200° C. (atmosphere atmosphere) for 1 hour. As a result, a porous protective layer of about 300 ⁇ m was formed on the inner surface of the metal 2. Then, the step of immersing the metal 2 in the raw material slurry and drying it was repeated 3 times to form a 1.2 mm porous protective layer on the inner surface of the metal 2. Then, the metal 2 was placed in an electric furnace and fired at 800° C. (atmosphere atmosphere) for 3 hours to prepare a composite member 10. The porous protective layer 4 was formed on the entire inner surface of the metal 2 (see FIG. 3).
- the porosity of the porous protective layer 4 was 61% by volume and the thermal expansion coefficient was 7 ⁇ 10 ⁇ 6 K ⁇ 1 .
- the titania particles are present between the surface (inner surface) of the metal 2 and the aggregate (alumina fibers and plate-like alumina particles) to form the surface of the metal 2 and the aggregate. It was confirmed that they were joined.
- the porous protective layer 4 is bonded to the inner surface and the outer surface of the metal 2.
- the composite member 10a was manufactured through substantially the same steps as the composite member 10 without masking the metal 2.
- the porous protective layer 4 was formed on the entire inner surface and outer surface of the metal 2.
- the porous protective layer 4 is bonded to the outer surface of the metal 2.
- the composite member 10b was manufactured through substantially the same steps as the composite member 10 with the inner surface of the metal 2 masked.
- the porous protective layer 4 was formed on the entire outer surface of the metal 2.
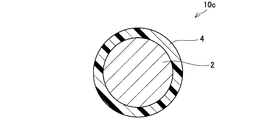
- the metal 2 is linear (line-shaped) and no hole is formed at the center (see FIGS. 1 to 5 for comparison). That is, in the composite member 10c, the metal 2 is solid.
- the porous protective layer 4 is bonded to the outer surface of the metal 2.
- the composite member 10c was manufactured through substantially the same steps as the composite member 10 without masking the metal 2.
- the porous protective layer 4 was formed on the entire inner surface and outer surface of the metal 2.
- the composite members 210 to 810 differ from the composite members 10 (and 10a to 10c) in the shape of the metal, the formation position or range of the porous protective layer, and the presence or absence of the coating layer.
- the composite members 210 to 810 were adjusted according to the purpose such as the masking position, the conditions for forming the porous protective layer, and the firing conditions after the porous protective layer was formed. It was manufactured through the same process. In the following description, description of features common to the composite member 10 (and 10a to 10c) may be omitted.
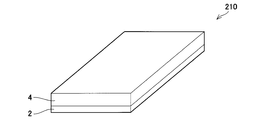
- the porous protective layer 4 is bonded to the surface of the flat metal 2 (one of the end faces in the thickness direction).
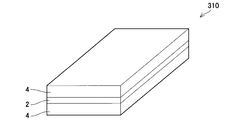
- the porous protective layer 4 is bonded to both surfaces (both surfaces of the end face in the thickness direction) of the flat metal plate 2.
- the composite members 210 and 310 can be suitably used as a material for a heat conducting member described later.
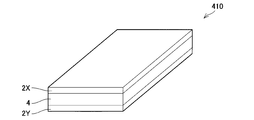
- metal plates (first metal plate 2X, second metal plate 2Y) are joined to both surfaces (front and back surfaces) of the porous protective layer 4.
- one porous protective layer 4 is connected to two metal plates (first metal plate 2X, second metal plate 2Y) facing each other with a gap.
- the composite member 410 can be suitably used as a partition plate arranged between two devices.
- the first metal plate 2X and the second metal plate 2Y can radiate heat generated from each device.
- heat of one device for example, device arranged on the first metal plate 2X side
- the other device (device arranged on the second metal plate 2Y side). Can be suppressed.
- the composite member 510 (fifth embodiment) shown in FIG. 10 is a modified example of the composite member 10c (see FIG. 6).
- the end portions (both end portions) 2a of the linear metal 2 in the longitudinal direction are exposed. That is, in the composite member 510, the porous protective layer 4 is joined to the intermediate portion of the metal 2 excluding the end portion 2a.
- the composite member 510 can be suitably used as a heat conducting member that transfers the heat of one end 2a to the other end 2a.
- the composite member 510 is provided with the porous protective layer 4 in the middle portion, it is possible to prevent heat from being applied to the components existing around the middle portion.
- the characteristics of the composite member 510 (the porous protective layer is bonded to the intermediate portion of the metal except the longitudinal end portions) can also be applied to the composite members 10, 10a, and 10b.
- a composite member 610 (sixth embodiment) shown in FIG. 11 is a modified example of the composite member 310 (see FIG. 8).
- the porous protective layer 4 is bonded to the entire surface of one surface (back surface) of the flat metal 2, and the other surface (front surface) has ends in the longitudinal direction (both ends) of the metal 2. ) It is joined to the intermediate part except 2a.
- the composite member 610 can be suitably used as a heat conducting member that transfers the heat of one end 2a to the other end 2a.
- the porous protective layer 4 may be bonded to both sides of the metal 2 to an intermediate portion of the metal 2 excluding the end 2a. Further, the characteristics of the composite member 610 (the porous protective layer is bonded to the intermediate portion of the metal except the longitudinal ends) can also be applied to the composite member 210.
- a composite member 710 (seventh embodiment) shown in FIG. 12 is a modified example of the composite member 210 (see FIG. 7).
- the coating layer 6 is provided on the surface of the porous protective layer 4 (the surface opposite to the surface on which the metal 2 is provided).
- the coating layer 6 was formed by forming the porous protective layer 4 on the surface of the metal 2, applying the raw material slurry on the surface of the porous protective layer 4 using a spray, and drying and firing.
- the raw material slurry used for forming the coating layer 6 is plate-like alumina particles (average particle size 6 ⁇ m), titania particles (average particle size 0.25 ⁇ m), alumina sol (alumina amount 1.1% by mass), Acrylic resin (average particle diameter 8 ⁇ m) and ethanol were mixed to prepare. That is, the raw material slurry used for forming the coating layer 6 is obtained by removing alumina fibers from the raw material slurry used for forming the porous protective layer 4.
- the coating layer 6 has a denser structure than the porous protective layer 4, and thus functions as a reinforcing material for the porous protective layer 4.
- the material of the coating layer 6 can be appropriately changed to, for example, the above-mentioned material according to the purpose.
- a composite member 810 (eighth embodiment) shown in FIG. 13 is a modified example of the composite member 710 (see FIG. 12).
- the coating layer 6 is intermittently (partially) provided on the surface of the porous protective layer 4 in the longitudinal direction of the composite member 810.
- the coating layer 6 is peeled from the porous protective layer 4 by intermittently providing the coating layer 6 on the surface of the porous protective layer 4.
- the characteristics of the composite members 710, 810 (providing a coating layer on the surface of the porous protective layer) can also be applied to the composite members 10, 10a to 10c, 210, 310, 510 and 610.
- heat conduction member 910 An example of using the above-described composite member (heat conduction member 910) will be described with reference to FIG. 14. Note that the heat conducting member 910 uses the composite member 610 (see FIG. 11), but instead of the composite member 610, the other composite member described above can be used.
- the porous protective layer 4 is joined to the entire back surface of the metal 2 and also to the middle portion (the portion excluding the end portion 2a in the longitudinal direction) of the front surface of the metal 2. That is, with respect to the surface of the metal 2, the porous protective layer 4 is not bonded to the end portion 2.
- the heat generating portion 20 and the heat radiating portion 22 are joined to the end portion 2a.
- the heat received by the heat generating portion 20 moves through the metal 2 and is radiated by the heat radiating portion 22 (heat radiating plate). Since the porous protective layer 4 is bonded to the front surface (intermediate portion) and the back surface of the heat conducting member 910, heat radiation from the metal 2 is suppressed between the heat generating portion 20 and the heat radiating portion 22. Therefore, it is possible to prevent heat from being applied to the devices provided in the space 30 near the front surface of the heat conducting member 910 and the space 32 near the back surface of the heat conducting member 910.
- the porous protective layer is a raw material slurry prepared by mixing alumina fibers, plate-like alumina particles, titania particles, alumina sol, acrylic resin and ethanol, and after immersing the metal in the raw material slurry, drying and firing.
- alumina fibers alumina fibers
- titania particles alumina sol
- acrylic resin acrylic resin
- ethanol alumina sol
- ethanol alumina sol
- ethanol ethanol
- the amount of alumina fibers, tabular alumina particles, titania particles, and zirconia particles is changed as shown in FIG. 15, and the total amount of alumina fibers, tabular alumina particles, titania particles, and zirconia particles is 100% by mass.
- 10 mass% of alumina sol (1.1 mass% of alumina contained in alumina sol) and 40 mass% of acrylic resin are added by external coating, and the slurry viscosity is adjusted with ethanol to prepare a raw material slurry. did.
- Sample 5 does not use plate-like alumina particles, and Samples 1 to 7, 11 and 13 do not use zirconia particles.
- the raw material slurry was applied to a SUS430 plate, and for Samples 9 and 10, the raw material slurry was applied to a copper plate and dried at 200° C. for 1 hour in an atmospheric atmosphere. Calcination was carried out for 3 hours. The number of times the raw material slurry was applied to each sample (the number of times the metal plate was immersed) was adjusted so that a porous protective layer of about 1.2 mm was formed on the metal plate (SUS430 plate and copper plate).
- this experimental example aims to confirm the influence (whether cracks, peeling, etc.) of the alumina component (alumina fiber, plate-like alumina particles) and the amount of the titania component on the appearance of the porous protective layer. The heat insulation of the porous layer was not evaluated.
- the ratio (mass%) of the alumina component and the titania component in the porous protective layer, the porosity (volume%) of the porous protective layer, the porous protective layer and the metal were measured.
- the coefficient of thermal expansion of the plate was also measured.
- Alumina and titania components are the results obtained by measuring the amounts of aluminum and titanium using an ICP emission analyzer (PS3520UV-DD manufactured by Hitachi High-Tech Science Co., Ltd.) and converting them into oxides (Al 2 O 3 , TiO 2 ). ing.
- the porosity was measured by using a mercury porosimeter in accordance with JIS R1655 (a method for testing the pore size distribution of a molded body by the mercury intrusion method for fine ceramics), and the total pore volume (unit: cm 3 /g) and the gas substitution formula
- the apparent density (unit: g/cm 3 ) measured with a densitometer (Acupic 1330, manufactured by Micromeritics) was used to calculate from the following formula (2).
- the above raw material slurry was molded into a bulk body of 3 mm x 4 mm x 20 mm, and then the bulk body was fired at 800°C to prepare a measurement sample. Then, the measurement sample was measured using a thermal expansion meter in accordance with JIS R1618 (a method for measuring thermal expansion by thermomechanical analysis of fine ceramics). The coefficient of thermal expansion was measured separately for the porous protective layer and the metal plate.
- the thermal conductivity of the porous protective layers of Samples 1 to 4 and the metal plates of Samples 1 to 12 was measured.
- the thermal conductivity was also measured separately for the porous protective layer and the metal plate.
- the thermal conductivity was calculated by multiplying the thermal diffusivity, the specific heat capacity and the bulk density.
- the thermal diffusivity was measured using a laser flash method thermal constant measuring device, and the specific heat capacity was measured using a DSC (differential scanning calorimeter) according to JIS R1611 (thermal diffusivity/specific heat capacity/thermal conductivity test by laser flash method of fine ceramics). According to the method), the measurement was performed at room temperature.
- the bulk density of the metal plate was obtained by measuring the weight of a bulk body having a diameter of 10 mm and a thickness of 1 mm, and dividing the weight by the volume to obtain a bulk density (unit: g/cm 3 ).
- the bulk density (unit: cm 3 /g) of the porous protective layer was calculated from the following formula (3).
- the thermal diffusivity was obtained by forming the raw material slurry described above into a bulk body having a diameter of 10 mm and a thickness of 1 mm, and the specific heat capacity was obtained by forming the raw material slurry described above into a bulk body having a diameter of 5 mm and a thickness of 1 mm.
- the proportion of the alumina component of Sample 11 is less than 15% by mass, the bonding force between the ceramics (particles and fibers) is reduced, and it is presumed that the porous protective layer was cracked. Further, in Sample 12, since the proportion of the titania component was less than 45% by mass, it is presumed that the bonding force between the ceramics was reduced and cracks were generated in the porous protective layer. Further, since the sample 12 has a low content of the titania component (titania particles) having a high thermal expansion coefficient and a small thermal expansion coefficient ratio ( ⁇ 1/ ⁇ 2) to the metal (less than 0.5), it is between the metal and the porous protective layer. It is presumed that the porous protective layer was separated from the metal based on the difference in thermal expansion. From the above, it was confirmed that the porous protective layer containing 15% by mass or more of the alumina component and 45% by mass or more of the titania component was less prone to deterioration such as cracking and peeling after firing.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- General Engineering & Computer Science (AREA)
- Structural Engineering (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Metallurgy (AREA)
- Manufacturing & Machinery (AREA)
- Inorganic Chemistry (AREA)
- Laminated Bodies (AREA)
- Other Surface Treatments For Metallic Materials (AREA)
- Cooling Or The Like Of Semiconductors Or Solid State Devices (AREA)
- Cooling Or The Like Of Electrical Apparatus (AREA)
Abstract
複合部材は、金属の表面に無機多孔質層が設けられている。無機多孔質層は、セラミックス繊維を含んでいる。また、無機多孔質層は、15質量%以上のアルミナ成分と45質量%以上のチタニア成分によって構成されている。
Description
本明細書は、複合部材に関する技術を開示する。
金属の表面に無機質の保護層を設け、金属と無機材料の複合部材を構成することがある。例えば、特開2018-33245号公報(以下、特許文献1と称する)は、主に自動車のエンジン部品(金属)に耐熱性を付与するため、金属表面に無機保護層を被覆している。特許文献1では、金属と無機保護層の熱膨張率の相違に伴って無機保護層が金属から剥離することを防止するため、金属表面に非晶性無機材層(具体的には、硼珪酸ガラス)を形成し、非晶性無機材層の表面に非酸化物系セラミックス(具体的には、炭化ケイ素)を形成している。すなわち、特許文献1では、金属と、保護層としての機能を発揮する機能層(炭化ケイ素)との間に、両者の熱膨張率差を緩和するための緩和層(硼珪酸ガラス)を設けている。特許文献1は、非晶質の緩和層を設けることにより、金属と機能層の密着性を向上させている。
上記したように、特許文献1は、金属と機能層の間に非晶質の緩和層を設ける。そのため、機能層を形成する際、緩和層の軟化点を超えない温度で機能層を形成することが必要である。換言すると、機能層として利用可能な材料が、緩和層の軟化点を超えない条件で成膜可能な材料に制限される。そのため、特許文献1の複合部材は、使用し得る材料(緩和層、機能層)の自由度が低い。また、特許文献1の複合部材は、非晶質の緩和層を用いているので、耐熱性の向上も限定的である。そのため、複合材料の分野においては、継続的な改善が必要とされている。本明細書は、従来にない新規な複合部材を提供することを目的とする。
本明細書で開示する複合材料は、金属の表面に無機多孔質層が設けられていてよい。また、無機多孔質層は、セラミックス繊維を含んでいてよい。さらに、無機多孔質層は、15質量%以上のアルミナ成分と、45質量%以上のチタニア成分によって構成されていてよい。上記したように、この複合材料では、無機多孔質層がセラミックス繊維を含んでいる。そのため、無機多孔質層自体が、金属と無機多孔質層の熱膨張率差の影響を吸収することができる。具体的には、無機多孔質層が金属の変形(熱膨張,熱収縮)に追従して変形することができるので、金属と無機多孔質層の間に緩和層(非晶質層等)を設けることなく、金属から無機多孔質層が剥離することを防止することができる。
また、上記複合部材は、金属の表面に無機の「多孔質層」が設けられている。典型的に、多孔質体は、多孔質体を介した内外の環境を「断つ」能力が高い。そのため、上記複合部材は、外部環境が金属に影響を及ぼすことを抑制し、あるいは、外部環境に金属の影響が及ぶことを抑制し、高い断熱性、高い遮音性(吸音性)等を実現することができる。また、上記複合部材は、無機多孔質層によって、吸着性、吸湿性等、外部環境の物質(異物、水分等)が金属に接することを抑制することもできる。あるいは、上記複合部材は、無機多孔質層を利用して、触媒等を金属表面に担持させることもできる。なお、本明細書でいう「多孔質」とは、無機多孔質層の気孔率(空隙率)が45体積%以上であることを意味する。
上記複合部材は、無機多孔質層にセラミックス繊維が含まれているので、無機多孔質層自体の強度(機械的強度)が低下することが抑制されている。また、無機多孔質層は、15質量%以上のアルミナ成分と45質量%以上のチタニア成分によって構成されているので、無機多孔質層自体の融点が高く、複合部材の外部環境が高温になっても形状を維持することができる。
複合部材では、無機多孔質層の熱膨張係数をα1とし、金属の熱膨張係数をα2としたときに、下記式(1)を満足していてよい。無機多孔質層が金属から剥離する現象を、より確実に防止することができる。
式1:0.5<α1/α2<1.2
式1:0.5<α1/α2<1.2
複合部材では、無機多孔質層に板状セラミックス粒子が含まれていてよい。板状セラミックス粒子を用いることにより、セラミックス繊維の一部を板状セラミックス粒子に置換することができる。典型的に、板状セラミックス粒子の長さ(長手方向サイズ)は、セラミックス繊維の長さより短い。そのため、板状セラミックス粒子を用いることにより、無機多孔質層内の伝熱経路が分断され、無機多孔質層内の熱伝達が起こりにくくなる。その結果、無機多孔質層の断熱性能がさらに向上する。なお、「板状セラミックス粒子」とは、アスペクト比5以上で、長手方向サイズが5μm以上50μm以下のセラミックス粒子を意味する。
複合部材では、無機多孔質層に、0.1μm以上10μm以下の粒状粒子が含まれていてよい。無機多孔質層を成形(焼成)する際、セラミックス繊維同士が粒状粒子を介して結合され、高強度の無機多孔質層が得られる。また、無機多孔質層の厚みは、1mm以上であってよい。上記した機能(断熱性、遮音性、吸着性、吸湿性等)を十分に発揮することができる。なお、上記複合部材は、無機多孔質層がセラミックス繊維を含んでいるので、1mm以上の無機多孔質層を実現することができる。すなわち、無機多孔質層を成形する過程(例えば、焼成工程)において収縮が起こり難いセラミックス繊維を含むので、無機多孔質層を1mm以上に成形することができる。例えば、無機多孔質層がセラミックス繊維を含んでいない場合、成形する過程で無機多孔質層が収縮し、クラック等が発生する、そのため、無機多孔質層がセラミックス繊維を含んでいない場合、無機多孔質層を1mm以上という厚膜に形成することが困難である。
以下、本明細書で開示される複合部材の実施形態を説明する。本明細書で開示する複合部材は、金属の表面に無機多孔質層が設けられている。また、無機多孔質層は、セラミックス繊維を含んでいる。また、無機多孔質層は、15質量%以上55質量%以下のアルミナ(Al2O3)成分と、45質量%以上85質量%以下のチタニア(TiO2)成分によって構成されている。なお、無機多孔質層に含まれるアルミナ成分は、25質量%以上であってよく、30質量%以上であってよく、40質量%以上であってもよい。本明細書で開示する複合部材は、例えば、高温環境下において好適に用いることができる。一例として、複合部材は、エキゾーストマニホールド、エキゾーストパイプといった自動車の排気系を構成する部材として好適に用いることができる。また、本明細書で開示する複合部材は、例えば、熱源で生じた熱を熱源から離れた位置に存在する部品(例えば放熱板)に伝達する熱伝導部材として好適に用いることができる。あるいは、複数の機器の間に複合部材を配置し、一方の機器から生じる熱が他方の機器に加わることを防止する仕切り板として好適に用いることもできる。
無機多孔質層は、金属表面を被覆し、金属を外部環境から保護してよい。なお、「外部環境」とは、無機多孔質層を介して金属の反対側の空間のことを意味する。すなわち、複合材料が上記したような自動車の排気系を構成する部材の場合、「外部環境」は、エキゾーストマニホールド、エキゾーストパイプ等の内部空間に相当する。あるいは、無機多孔質層は、金属表面を被覆し、複合部材の外部環境に存在する部品を、金属の熱から保護(断熱)してよい。また、無機多孔質層は、間隔をあけて対向する2個の金属(例えば金属板)の双方の表面を被覆していてもよい。換言すると、1個の無機多孔質層の両面に、金属板(第1金属板,第2金属板)が接合されていてもよい。第1金属板側に配置されている第1機器から生じる熱が第2金属板側に配置されている第2機器に加わることを防止することができるとともに、第1金属板によって、第1機器が生じた熱を放熱することができる。
上記したように、複合部材は、無機多孔質層によって、金属と外部環境が互いに熱の影響を及ぼし合うことを抑制する。また、無機多孔質層によって、複数の機器が配置される空間を分離し、分離された空間同士が熱の影響を及ぼし合うことを抑制する。そのため、金属と無機多孔質層は、熱伝導率の差が大きいことが好ましい。具体的には、金属の熱伝導率は、無機多孔質層の熱伝導率の100倍以上であってよい。なお、金属の熱伝導率は、無機多孔質層の熱伝導率の150倍以上であってよく、無機多孔質層の熱伝導率の200倍以上であってよく、無機多孔質層の熱伝導率の250倍以上であってよく、無機多孔質層の熱伝導率の300倍以上であってもよい。
金属の熱伝導率は、10W/mK以上400W/mK以下であってよい。なお、金属の熱伝導率は、25W/mK以上であってよく、50W/mK以上であってよく、100W/mK以上であってよく、150W/mK以上であってよく、200W/mK以上であってよく、250W/mK以上であってよく、300W/mK以上であってよく、380W/mK以上であってもよい。また、金属の熱伝導率は、350W/mK以下であってよく、300W/mK以下であってよく、250W/mK以下であってよく、200W/mK以下であってよく、150W/mK以下であってもよい。
無機多孔質層の熱伝導率は、0.05W/mK以上3W/mK以下であってよい。なお、無機多孔質層の熱伝導率は、0.1W/mK以上であってよく、0.2W/mK以上であってよく、0.3W/mK以上であってよく、0.5W/mK以上であってよく、0.7W/mK以上であってよく、1W/mK以上であってよく、1.5W/mK以上であってよく、2W/mK以上であってもよい。また、無機多孔質層の熱伝導率は、2.5W/mK以下であってよく、2.0W/mK以下であってよく、1.5W/mK以下であってよく、1W/mK以下であってよく、0.5W/mK以下であってよく、0.3W/mK以下であってよく、0.25W/mK以下であってもよい。
金属の形状は、特に限定されないが、管状(筒状)、線状(ワイヤー状)、板状(シート状)であってよい。管状金属の場合、無機多孔質層は、管状金属の内周面、及び/又は、外周面を被覆していてよい。線状の金属は、典型的に中実構造である。そのため、線状金属の場合、無機多孔質層は、線状金属の外周面を被覆していてよい。板状金属の場合、無機多孔質層は、板状金属の露出面全体を被覆していてもよいし、厚み方向端部の面(表面、及び/又は、裏面)を被覆していてもよいし、幅方向端部の面(側面)を被覆していてもよいし、長さ方向端部の面を被覆していてもよい。また、板状金属の場合、無機多孔質層は、第1の板状金属(第1金属板)の表面と第2の板状金属(第2金属板)の裏面の双方を被覆していてよい。
無機多孔質層は、金属表面の全面を被覆していてもよいし、金属表面の一部を被覆していてもよい。例えば、無機多孔質層が管状金属,線状金属を被覆している場合、無機多孔質層は、金属の端部(一端または両端)を除く部分を被覆していてよい。また、無機多孔質層が管状金属の内周面及び外周面を被覆している場合、内周面は一端から他端まで無機多孔質層が被覆され(すなわち、全面被覆)、外周面は端部を除く部分が被覆されている等、内周面と外周面において無機多孔質層で被覆されている範囲が異なっていてもよい。また、無機多孔質層が板状金属を被覆している場合(例えば、厚み方向端部の面:表裏面)、無機多孔質層は、表裏面の一部(例えば、長手方向の一端または両端部)を除く部分を被覆していてよい。あるいは、無機多孔質層は、裏面については全体を被覆し、表面については例えば両端部を除く部分を被覆している等、表裏面で被覆する範囲が異なっていてもよい。
また、無機多孔質層は、厚み方向(金属表面と接する面から外部環境に露出する面に至る範囲)において、均一の材料で構成されていてよい。すなわち、無機多孔質層は単層であってよい。また、無機多孔質層は、厚み方向において、組成の異なる複数の層で構成されていてもよい。すなわち、無機多孔質層は、複数の層が積層した多層構造であってよい。あるいは、無機多孔質層は、厚み方向において、組成が除々に変化する傾斜構造であってもよい。無機多孔質層が単層の場合、複合部材の製造(金属表面に無機多孔質層を成形する工程)を容易に行うことができる。無機多孔質層が多層又は傾斜構造の場合、厚み方向において、無機多孔質層の特性を変化させることができる。無機多孔質層の構造(単層、多層、傾斜構造)については、複合部材の使用目的に応じて適宜選択することができる。
無機多孔質層の気孔率は、45体積%以上90体積%以下であってよい。気孔率が45体積%以上であれば、断熱性、遮音性、吸着性、吸湿性等、多孔質であることの機能を十分に発揮し得る。また、気孔率が45体積%以上であれば、無機多孔質層内の空隙を利用して、触媒を十分に担持させることもできる。気孔率が90体積%以下であれば、十分な強度を確保することができる。なお、無機多孔質層の気孔率は、55体積%以上であってよく、60体積%以上であってよく、65体積%以上であってもよい。さらに、無機多孔質層の気孔率は、85体積%以下であってよく、80体積%以下であってよく、70体積%以下であってよく、65体積%以下であってよく、60体積%以下であってもよい。また、無機多孔質層が多層構造又は傾斜構造の場合、無機多孔質層の気孔率は、全体として45体積%以上90体積%以下であればよく、厚み方向で気孔率が異なっていてもよい。この場合、部分的に、気孔率が45体積%未満の部分、あるいは、気孔率が90体積%超の部分が存在していてよい。
無機多孔質層の厚みは、使用目的(要求性能)に依るが、1mm以上であってよい。無機多孔質層の厚みが1mm以上であれば、断熱性、遮音性、吸着性、吸湿性等、多孔質であることの機能を十分に発揮し得る。なお、セラミックス繊維が用いられていない無機多孔質層の場合、製造過程(例えば焼成工程)において収縮するため、厚みを1mm以上に維持することが困難である。本明細書で開示する無機多孔質層は、セラミックス繊維を含んでいるので、製造過程における収縮が抑制され、1mm以上の厚みを維持することができる。なお、無機多孔質層の厚みが厚すぎると、コスト(製造コスト、材料コスト)に見合う特性の向上が得られにくくなる。そのため、特に限定されないが、無機多孔質層の厚みは、30mm以下であってよく、20mm以下であってよく、15mm以下であってよく、100mm以下であってよく、5mm以下であってよい。
無機多孔質層は、セラミックス粒子(粒状粒子)、板状セラミックス粒子、セラミックス繊維のうちの1以上の材料により構成されている。なお、セラミックス粒子、板状セラミックス粒子及びセラミックス繊維は、構成成分として、アルミナ、及び/又は、チタニアを含んでいてよい。換言すると、アルミナ、及び/又は、チタニアによって、セラミックス粒子、板状セラミックス粒子、セラミックス繊維が形成されていてよい。すなわち、無機多孔質層は、構成材料(構成物質)全体で、15質量%以上のアルミナ成分と45質量%以上のチタニア成分を含んでいればよい。但し、無機多孔質層は、構成成分は任意(アルミナ成分、チタニア成分を含んでいてもよいし、含んでいなくてもよい)であるが、少なくともセラミックス繊維を含んでいる。
セラミックス粒子は、板状セラミックス粒子,セラミックス繊維等の無機多孔質層の骨格をなす骨材同士を接合する接合材として用いられてよい。セラミックス粒子は、0.1μm以上10μm以下の粒状粒子であってよい。なお、セラミックス粒子は、製造過程(例えば焼成工程)において、焼結等により粒径が大きくなってもよい。すなわち、無機多孔質層を製造する原料として、セラミックス粒子は、0.1μm以上10μm以下(焼成前の平均粒径)の粒状粒子であってよい。なお、セラミックス粒子は、0.5μm以上であってよく、5μm以下であってもよい。セラミックス粒子の材料として、例えば金属酸化物を利用してよい。金属酸化物の一例として、アルミナ(Al2O3)、スピネル(MgAl2O4)、チタニア(TiO2)、ジルコニア(ZrO2)、マグネシア(MgO)、ムライト(Al6O13Si2)、コージェライト(MgO・Al2O3・SiO2)、イットリア(Y2O3)、ステアタイト(MgO・SiO2)フォルステライト(2MgO・SiO2)、ランタンアルミネート(LaAlO3)、ストロンチウムチタネート(SrTiO3)等が挙げられる。これらの金属酸化物は、高い耐蝕性を有する。そのため、セラミックス粒子の材料として上記金属酸化物を用いることにより、無機多孔質層を、例えば自動車の排気系を部品(エキゾーストマニホールド等)の保護層として好適に適用することができる。
板状セラミックスは、無機多孔質層内において、骨材、補強材として機能し得る。すなわち、板状セラミックスは、セラミックス繊維と同様に、無機多孔質層の強度を向上させ、さらに、製造工程において無機多孔質層が収縮することを抑制する。なお、板状セラミックス粒子を用いることにより、無機多孔質層内の伝熱経路を分断することができる。そのため、複合部材が高温環境で用いられる場合(無機多孔質層が金属を断熱する目的で用いられる場合)、骨材としてセラミックス繊維のみを用いる形態と比較して、断熱性を向上させることができる。
板状セラミックス粒子は、矩形板状、あるいは、針状であってよく、長手方向サイズが5μm以上100μm以下であってよい。長手方向サイズが5μm以上であれば、セラミックス粒子の過剰な焼結を抑制することができる。長手方向サイズが100μm以下であれば、上述したように無機多孔質層内の伝熱経路を分断する効果が得られ、高温環境で用いる複合部材に好適に適用し得る。また、板状セラミックス粒子は、アスペクト比が5以上100以下であってよい。アスペクト比が5以上であればセラミックス粒子の焼結を良好に抑制することができ、100以下であれば板状セラミックス粒子自体の強度低下が抑制される。なお、板状セラミックス粒子の材料として、上記したセラミックス粒子の材料として用いられる金属酸化物に加え、タルク(Mg3Si4O10(OH)2)、マイカ、カオリン等の鉱物・粘土、ガラス等を用いることもできる。
セラミックス繊維は、無機多孔質層内において、骨材、補強材として機能し得る。すなわち、セラミックス繊維は、無機多孔質層の強度を向上させ、さらに、製造工程において無機多孔質層が収縮することを抑制する。セラミックス繊維の長さは、50μm以上200μm以下であってよい。また、セラミックス繊維の直径(平均径)は、1~20μmであってよい。無機多孔質層内におけるセラミックス繊維の体積率(無機多孔質層を構成する材料に占めるセラミックス繊維の体積率)は、5体積%以上25体積%以下であってよい。5体積%以上のセラミックス繊維を含むことにより、無機多孔質層の製造過程(焼成工程)において無機多孔質層内のセラミックス粒子の収縮を十分に抑制することができる。また、セラミックス繊維の体積率を25体積%以下とすることにより、無機多孔質層内の伝熱経路を分断することができ、高温環境で用いる複合部材に好適に適用し得る。なお、セラミックス繊維の材料として、上述した板状セラミックス粒子の材料と同様の材料を用いることができる。
また、無機多孔質層内における骨材、補強材(セラミックス繊維,板状セラミックス粒子等。以下、単に骨材と称する)の含有率は、15質量%以上55質量%以下であってよい。無機多孔質層内の骨材の含有率が15質量%以上であれば、焼成工程における無機多孔質層の収縮を十分に抑制することができる。また、無機多孔質層内の骨材の含有率が55質量%以下であれば、セラミックス粒子によって骨材同士が良好に接合される。無機多孔質層内における骨材の含有率は、20質量%以上であってよく、30質量%以上であってよく、50質量%以上であってよく、53質量%以上であってもよい。また、無機多孔質層内における骨材の含有率は、53質量%以下であってよく、50質量%以下であってよく、30質量%以下であってよく、20質量%以下であってもよい。
上記したように、セラミックス繊維及び板状セラミックス粒子は、ともに無機多孔質層内において骨材、補強材として機能し得る。しかしながら、複合部材の作製後(焼成後)に無機多孔質層が収縮することを確実に抑制するため、骨材としてセラミックス繊維と板状セラミックス粒子の双方を用いる場合であっても、無機多孔質層内のセラミックス繊維の含有量は、少なくとも5質量%以上であってよい。なお、セラミックス繊維の含有量は、10質量%以上であってよく、20質量%以上であってよく、30質量%以上であってよく、40質量%以上であってよい。また、セラミックス繊維の含有量は、50質量%以下であってよく、40質量%以下であってよく、30質量%以下であってよく、20質量%以下であってよく、10質量%以下であってもよい。
骨材としてセラミックス繊維と板状セラミックス粒子の双方を用いる場合、骨材全体に占める板状セラミックス粒子の割合(重量比)は、70%以下であってよい。すなわち、質量比で、骨材の少なくとも30%以上がセラミックス繊維であってよい。骨材全体に占める板状セラミックス粒子の割合(重量比)は、67%以下であってよく、64%以下であってよく、63%以下であってよく、60%以下であってよく、50%以下であってもよい。なお、板状セラミックス粒子は必ずしも骨材として必須ではない。また、骨材全体に占める板状セラミックス粒子の割合は、40%以上であってよく、50%以上であってよく、60%以上であってよく、62%以上であってよく、63%以上であってよく、65%以上であってもよい。具体的には、無機多孔質層内の板状セラミックス粒子の含有量は、5質量%以上であってよく、10質量%以上であってよく、20質量%以上であってよく、30質量%以上であってよく、33質量%以上であってよい。また、板状セラミックス粒子の含有量は、35質量%以下であってよく、33質量%以下であってよく、30質量%以下であってよく、20質量%以下であってよく、10質量%以下であってもよい。
なお、特に高温環境で用いられる複合部材においては、無機多孔質層に含まれるSiO2が25質量%以下であってよい。無機多孔質層内に非晶質層が形成されることが抑制され、無機多孔質層の耐熱性(耐久性)が向上する。
無機多孔質層を形成する際、セラミックス粒子、板状セラミックス粒子、セラミックス繊維の他に、バインダ、造孔材、溶媒を混合した原料を用いてよい。バインダとして、無機バインダを使用してよい。無機バインダの一例として、アルミナゾル、シリカゾル、チタニアゾル、ジルコニアゾル等が挙げられる。これらの無機バインダは、焼成後の無機多孔質層の強度を向上させることができる。造孔材として、高分子系造孔材、カーボン系粉等を使用してよい。具体的には、アクリル樹脂、メラミン樹脂、ポリエチレン粒子、ポリスチレン粒子、カーボンブラック粉末、黒鉛粉末等が挙げられる。造孔材は、目的に応じて種々の形状であってよく、例えば、球状、板状、繊維状等であってよい。造孔材の添加量、サイズ、形状等を選択することにより、無機多孔質層の気孔率、気孔サイズを調整することができる。溶媒は、他の原料に影響を及ぼすことなく原料の粘度を調整可能なものであればよく、例えば、水、エタノール、イソプロピルアルコール(IPA)等を使用することができる。
なお、上記した無機バインダも無機多孔質層の構成材料である。そのため、無機多孔質層を形成する際にアルミナゾル、チタニアゾル等を用いる場合、無機多孔質層は、無機バインダを含む構成材料全体で、15質量%以上のアルミナ成分と45質量%以上のチタニア成分を含んでいればよい。
無機多孔質層の組成及び原料は、保護する金属の種類に応じて調整する。本明細書で開示する複合部材では、特に限定されないが、金属として、SUS430,SUS429,SUS444等のステンレス鋼、鉄、銅、ハステロイ、インコネル、コバール、ニッケル合金等を用いることができる。無機多孔質層の組成及び原料は、用いる金属の熱膨張係数に応じて調整してよい。具体的には、無機多孔質層の熱膨張係数をα1とし、金属の熱膨張係数をα2としたときに、下記式1を満足するように調整してよい。例えば、金属がSUS430の場合、熱膨張係数α1が6×10⁻⁶/K<α1<14×10-6/Kとなるように、より好ましくは、熱膨張係数α1が6×10-6/K<α1<11×10-6/Kとなるように、無機多孔質層の組成及び原料を調整してよい。また、金属が銅の場合、熱膨張係数α1が8.5×10-6/K<α1<20×10-6/Kとなるように、より好ましくは、熱膨張係数α1が8.5×10-6/K<α1<18×10-6/Kとなるように、無機多孔質層の組成及び原料を調整してよい。なお、「α1/α2」の値は、0.55以上であってよく、0.6以上であってよく、0.65以上であってよく、0.75以上であってよく、0.8以上であってもよい。また、「α1/α2」の値は、1.15以下であってよく、1.1以下であってよく、1.05以下であってよく1.0以下であってもよい。
式1:0.5<α1/α2<1.2
式1:0.5<α1/α2<1.2
本明細書で開示する複合部材では、金属表面(管状金属の場合、管内)に上記原料を塗布し、乾燥、焼成を経て金属表面に無機多孔質層を形成してよい。原料の塗布方法として、ディップコート、スピンコート、スプレーコート、スリットダイコート、溶射、エアロゾルデポジション(AD)法、印刷、刷毛塗り、コテ塗り、モールドキャスト成形等を用いることができる。なお、目的とする無機多孔質層の厚みが厚い場合、あるいは、無機多孔質層が多層構造の場合、原料の塗布、原料の乾燥を複数回繰り返し、目的とする厚み、あるいは、多層構造に調整してもよい。上記塗布方法は、後述する被覆層を形成する塗布方法として適用することもできる。
また、本明細書で開示する複合部材では、無機多孔質層の金属が設けられている面とは反対側の面に、被覆層が設けられていてもよい。すなわち、無機多孔質層が、金属と被覆層によって挟まれていてよい。なお、被覆層は、無機多孔質層の表面(金属が設けられている面と反対側の面)の全面に設けられていてもよいし、無機多孔質層の表面の一部に設けられていてもよい。被覆層を設けることにより、無機多孔質層を保護(補強)することができる。
被覆層の材料は、多孔質または緻密質なセラミックスであってよい。被覆層で用いられる多孔質セラミックスの一例として、ジルコニア(ZrO2),部分安定化ジルコニア,安定化ジルコニア等が挙げられる。また、イットリア安定化ジルコニア(ZrO2-Y2O3:YSZ)、YSZにGd2O3、Yb2O3、Er2O3等を添加した金属酸化物、ZrO2-HfO2-Y2O3、ZrO2-Y2O3-La2O3、ZrO2-HfO2-Y2O3-La2O3、HfO2-Y2O3、CeO2-Y2O3、Gd2Zr2O7、Sm2Zr2O7、LaMnAl11O19、YTa3O9、Y0.7La0.3Ta3O9、Y1.08Ta2.76Zr0.24O9、Y2Ti2O7、LaTa3O9、Yb2Si2O7、Y2Si2O7、Ti3O5等が挙げられる。被覆層で用いられる緻密質なセラミックスの一例として、アルミナ、シリカ、ジルコニアなどが挙げられる。また、上述した無機多孔質層の構成材料からセラミックス繊維を除去することにより、低気孔率(緻密質)となるため、被覆層として用いてもよい。被覆層として多孔質または緻密質セラミックスを用いることにより、無機多孔質層が補強され、無機多孔質層が金属の表面から剥がれることを抑制することができる。なお、被覆層として緻密質なセラミックスを用いると、例えば高温ガスが無機多孔質層を透過することを抑制したり、無機多孔質層内で高温ガスが滞留することを抑制することができる。その結果、高温ガスの熱が金属に伝熱することを抑制する効果が期待できる。また、被覆層として緻密質なセラミックスを用いることにより、金属と外部環境を電気的に絶縁する効果が向上する。
被覆層の材料は、多孔質または緻密質なガラスであってよい。被覆層として多孔質または緻密質ガラスを用いることによっても、無機多孔質層が補強され、無機多孔質層が金属の表面から剥がれることを抑制することができる。また、被覆層の材料は、金属(無機多孔質層によって保護される金属とは別部品)であってもよい。無機多孔質層の表面に金属層を設けることにより、外部からの輻射熱を反射することができ、金属(無機多孔質層によって保護される金属)に熱が加わることをさらに抑制することができる。
(第1実施例)
図1から図3を参照し、複合部材10について説明する。複合部材10は、SUS430製の管状の金属(金属管)2の内面に多孔質保護層4を備えている。多孔質保護層4は、無機多孔質層の一例である。多孔質保護層4は、金属2の内面に接合している(図1及び図2を参照)。複合部材10は、金属2の外面をマスキングした状態で、金属2を原料スラリーに浸漬し、乾燥、焼成を行って製造した。原料スラリーは、アルミナ繊維(平均繊維長140μm)と、板状アルミナ粒子(平均粒子径6μm)と、チタニア粒子(平均粒子径0.25μm)と、アルミナゾル(アルミナ量1.1質量%)と、アクリル樹脂(平均粒子径8μm)と、エタノールを混合し、作成した。なお、原料スラリーは、粘度が2000mPa・sとなるように調整した。
図1から図3を参照し、複合部材10について説明する。複合部材10は、SUS430製の管状の金属(金属管)2の内面に多孔質保護層4を備えている。多孔質保護層4は、無機多孔質層の一例である。多孔質保護層4は、金属2の内面に接合している(図1及び図2を参照)。複合部材10は、金属2の外面をマスキングした状態で、金属2を原料スラリーに浸漬し、乾燥、焼成を行って製造した。原料スラリーは、アルミナ繊維(平均繊維長140μm)と、板状アルミナ粒子(平均粒子径6μm)と、チタニア粒子(平均粒子径0.25μm)と、アルミナゾル(アルミナ量1.1質量%)と、アクリル樹脂(平均粒子径8μm)と、エタノールを混合し、作成した。なお、原料スラリーは、粘度が2000mPa・sとなるように調整した。
金属2を上記原料スラリーに浸漬して金属2の内面に原料を塗布した後、金属2を乾燥機に投入し、200℃(大気雰囲気)で1時間乾燥させた。これにより、金属2の内面におよそ300μmの多孔質保護層が形成された。その後、金属2を上記原料スラリーに浸漬して乾燥する工程を3回繰り返し、金属2の内面に1.2mmの多孔質保護層を形成した。その後、金属2を電気炉内に配置し、800℃(大気雰囲気)で3時間焼成し、複合部材10を作成した。多孔質保護層4は、金属2の内面全体に形成された(図3を参照)。得られた複合部材10は、多孔質保護層4の気孔率が61体積%であり、熱膨張係数が7×10⁻⁶K-1であった。なお、図示は省略するが、複合部材10では、チタニア粒子が、金属2の表面(内面)と骨材(アルミナ繊維及び板状アルミナ粒子)の間に介在し、金属2の表面と骨材を接合していることが確認された。
図4から図6を参照し、複合部材10の変形例(複合部材10a、10b、10c)について説明する。なお、図4から図6は、複合部材10の図3(断面図)に相当する部分を示している。
図4に示すように、複合部材10aでは、多孔質保護層4が、金属2の内面及び外面に接合している。複合部材10aは、金属2にマスキングを施すことなく、複合部材10と実質的に同じ工程を経て製造した。多孔質保護層4は、金属2の内面及び外面の全体に形成された。
図5に示すように、複合部材10bでは、多孔質保護層4が、金属2の外面に接合している。複合部材10bは、金属2の内面をマスキングした状態で、複合部材10と実質的に同じ工程を経て製造した。多孔質保護層4は、金属2の外面の全体に形成された。
図6に示すように、複合部材10cは、金属2が線状(ライン状)であり、中心に孔が形成されていない(図1~図5を比較参照)。すなわち、複合部材10cでは、金属2が中実である。複合部材10cでは、多孔質保護層4が、金属2の外面に接合している。複合部材10cは、金属2にマスキングを施すことなく、複合部材10と実質的に同じ工程を経て製造した。多孔質保護層4は、金属2の内面及び外面の全体に形成された。
(第2~第8実施例)
以下、第2~第8実施例の複合部材(複合部材210~810)について説明する。複合部材210~810は、複合部材10(及び10a~10c)と比較して、金属の形状、多孔質保護層の形成位置または範囲、被覆層の有無が異なる。複合部材210~810は、マスキングを施す位置、多孔質保護層の形成条件、及び、多孔質保護層を形成した後の焼成条件等を目的に合わせて調整したが、実質的に複合部材10と同じ工程を経て製造した。以下の説明においては、複合部材10(及び10a~10c)と共通する特徴については説明を省略することがある。
以下、第2~第8実施例の複合部材(複合部材210~810)について説明する。複合部材210~810は、複合部材10(及び10a~10c)と比較して、金属の形状、多孔質保護層の形成位置または範囲、被覆層の有無が異なる。複合部材210~810は、マスキングを施す位置、多孔質保護層の形成条件、及び、多孔質保護層を形成した後の焼成条件等を目的に合わせて調整したが、実質的に複合部材10と同じ工程を経て製造した。以下の説明においては、複合部材10(及び10a~10c)と共通する特徴については説明を省略することがある。
図7に示す複合部材210(第2実施例)は、平板状の金属2の表面(厚み方向端面のうちの一方の面)に多孔質保護層4が接合している。図8に示す複合部材310(第3実施例)は、平板状の金属2の両面(厚み方向端面の双方の面)に多孔質保護層4が接合している。複合部材210,310は、後述する熱伝導部材の材料として好適に用いることができる。
図9に示す複合部材410(第4実施例)は、多孔質保護層4の両面(表裏面)に、金属板(第1金属板2X,第2金属板2Y)が接合している。換言すると、間隔をあけて対向する2個の金属板(第1金属板2X,第2金属板2Y)に、1個の多孔質保護層4が接続されている。複合部材410は、2個の機器の間に配置する仕切板として好適に用いることができる。第1金属板2X及び第2金属板2Yは、各機器から生じる熱を放熱することができる。また、多孔質保護層4は、一方の機器(例えば第1金属板2X側に配置されている機器)の熱が他方の機器(第2金属板2Y側に配置されている機器)に加わることを抑制することができる。
図10に示す複合部材510(第5実施例)は、複合部材10cの変形例である(図6を参照)。複合部材510は、線状の金属2の長手方向の端部(両端部)2aが露出している。すなわち、複合部材510は、金属2の端部2aを除く中間部分に多孔質保護層4が接合されている。複合部材510は、一方の端部2aの熱を他方の端部2aに伝達する熱伝導部材として好適に用いることができる。また、複合部材510は、中間部分に多孔質保護層4が設けられているので、中間部分の周囲に存在する部品に熱が加わることを抑制することができる。なお、複合部材510の特徴(金属の長手方向端部を除く中間部分に多孔質保護層が接合されている)は、複合部材10,10a及び10bに適用することもできる。
図11に示す複合部材610(第6実施例)は、複合部材310の変形例である(図8を参照)。複合部材610では、多孔質保護層4は、平板状の金属2の一方の面(裏面)の全面に接合されており、他方の面(表面)では金属2の長手方向の端部(両端部)2aを除く中間部分に接合されている。複合部材610は、複合部材510と同様に、一方の端部2aの熱を他方の端部2aに伝達する熱伝導部材として好適に用いることができる。なお、多孔質保護層4は、金属2の両面において金属2の端部2aを除く中間部分に接合されていてもよい。また、複合部材610の特徴(金属の長手方向端部を除く中間部分に多孔質保護層が接合されている)は、複合部材210に適用することもできる。
図12に示す複合部材710(第7実施例)は、複合部材210の変形例である(図7を参照)。複合部材710では、多孔質保護層4の表面(金属2が設けられている面とは反対側の面)に、被覆層6が設けられている。被覆層6は、金属2の表面に多孔質保護層4を形成した後、スプレーを用いて多孔質保護層4の表面に原料スラリーを塗布し、乾燥、焼成を経て成形した。被覆層6を成形するために用いた原料スラリーは、板状アルミナ粒子(平均粒子径6μm)と、チタニア粒子(平均粒子径0.25μm)と、アルミナゾル(アルミナ量1.1質量%)と、アクリル樹脂(平均粒子径8μm)と、エタノールを混合し、作成した。すなわち、被覆層6を成形するために用いた原料スラリーは、多孔質保護層4を形成するために用いた原料スラリーからアルミナ繊維を除去したものである。被覆層6は、多孔質保護層4と比較して緻密な構造を有しているので、多孔質保護層4の補強材として機能する。なお、被覆層6の材料は、目的に応じて、例えば上述した材料に適宜変更することができる。
図13に示す複合部材810(第8実施例)は、複合部材710の変形例である(図12を参照)。複合部材810では、被覆層6が、複合部材810の長手方向において、多孔質保護層4の表面に間欠的に(部分的に)設けられている。例えば、被覆層6と多孔質保護層4の熱膨張係数差が大きい場合、被覆層6を多孔質保護層4の表面に間欠的に設けることにより、被覆層6が多孔質保護層4から剥離することを抑制することができる。なお、複合部材710,810の特徴(多孔質保護層の表面に被覆層を設ける)は、複合部材10,10a~10c,210,310,510及び610に適用することもできる。
(熱伝導部材)
図14を参照し、上述した複合部材の使用例(熱伝導部材910)について説明する。なお、熱伝導部材910は、複合部材610(図11を参照)を用いているが、複合部材610に代えて、上述した他の複合部材を用いることもできる。熱伝導部材910では、多孔質保護層4は、金属2の裏面の全面に接合されているともに、金属2の表面の中間部分(長手方向の端部2aを除く部分)に接合されている。すなわち、金属2の表面については、端部2に多孔質保護層4が接合されていない。端部2aには発熱部20及び放熱部22が接合されている。発熱部20で受熱した熱は、金属2を移動し、放熱部22(放熱板)で放熱される。熱伝導部材910は、表面(中間部分)及び裏面に多孔質保護層4が接合されているので、発熱部20と放熱部22の間において金属2からの放熱が抑制される。そのため、熱伝導部材910の表面近傍の空間30、及び、熱伝導部材910の裏面近傍の空間32に設けられている機器に熱が加わることを抑制することができる。
図14を参照し、上述した複合部材の使用例(熱伝導部材910)について説明する。なお、熱伝導部材910は、複合部材610(図11を参照)を用いているが、複合部材610に代えて、上述した他の複合部材を用いることもできる。熱伝導部材910では、多孔質保護層4は、金属2の裏面の全面に接合されているともに、金属2の表面の中間部分(長手方向の端部2aを除く部分)に接合されている。すなわち、金属2の表面については、端部2に多孔質保護層4が接合されていない。端部2aには発熱部20及び放熱部22が接合されている。発熱部20で受熱した熱は、金属2を移動し、放熱部22(放熱板)で放熱される。熱伝導部材910は、表面(中間部分)及び裏面に多孔質保護層4が接合されているので、発熱部20と放熱部22の間において金属2からの放熱が抑制される。そのため、熱伝導部材910の表面近傍の空間30、及び、熱伝導部材910の裏面近傍の空間32に設けられている機器に熱が加わることを抑制することができる。
(実験例)
上記したように、多孔質保護層は、アルミナ繊維、板状アルミナ粒子、チタニア粒子、アルミナゾル、アクリル樹脂及びエタノールを混合した原料スラリーを作成し、金属を原料スラリーに浸漬させた後、乾燥及び焼成を行い作成した。本実験例では、アルミナ成分及びチタニア成分の量が多孔質保護層の特性に与える影響を確認するため、アルミナ繊維、板状アルミナ粒子及びチタニア粒子の割合を変化させ、焼成後の多孔質保護層の状態を確認した。
上記したように、多孔質保護層は、アルミナ繊維、板状アルミナ粒子、チタニア粒子、アルミナゾル、アクリル樹脂及びエタノールを混合した原料スラリーを作成し、金属を原料スラリーに浸漬させた後、乾燥及び焼成を行い作成した。本実験例では、アルミナ成分及びチタニア成分の量が多孔質保護層の特性に与える影響を確認するため、アルミナ繊維、板状アルミナ粒子及びチタニア粒子の割合を変化させ、焼成後の多孔質保護層の状態を確認した。
具体的には、アルミナ繊維、板状アルミナ粒子、チタニア粒子及びジルコニア粒子の配合量を図15に示すように変化させ、アルミナ繊維、板状アルミナ粒子、チタニア粒子及びジルコニア粒子の合計が100質量%になるように配合し、さらに、外掛けでアルミナゾル10質量%(アルミナゾルに含まれるアルミナ量1.1質量%)、アクリル樹脂40質量%を加え、エタノールでスラリー粘度を調整して原料スラリーを作成した。なお、試料5は板状アルミナ粒子を用いておらず、試料1~7,11及び13はジルコニア粒子を用いていない。その後、試料1~8,11及び12についてはSUS430板に原料スラリーを塗布し、試料9及び10については銅板に原料スラリーを塗布し、大気雰囲気200℃で1時間乾燥させた後、大気雰囲気800℃で3時間焼成した。なお、金属板(SUS430板及び銅板)上に約1.2mmの多孔質保護層が形成されるように、各試料における原料スラリーの塗布回数(金属板の浸漬回数)を調整した。
なお、本実験例は、アルミナ成分(アルミナ繊維、板状アルミナ粒子)及びチタニア成分の量が多孔質保護層の外観に及ぼす影響(クラック、剥離等の有無)を確認することを目的とし、無機多孔質層の断熱性の評価は行っていない。
焼成後の試料について、外観の評価を行った。外観評価は、目視にて、クラック及び剥離の発生の有無を観察した。図15に、クラック及び剥離等が発生しなかった試料に「〇」を付し、クラックと剥離の一方が発生した試料に「△」を付し、クラックと剥離の両方が発生した試料に「×」を付している。
また、作成した試料1~12について、多孔質保護層におけるアルミナ成分とチタニア成分の割合(質量%)の測定と、多孔質保護層の気孔率(体積%)の測定、多孔質保護層及び金属板の熱膨張係数の測定も行った。アルミナ及びチタニア成分は、ICP発光分析装置((株)日立ハイテクサイエンス製、PS3520UV-DD)を用いてアルミニウム及びチタン量を測定し、酸化物換算(Al2O3、TiO2)した結果を示している。
気孔率は、水銀ポロシメーターを用いてJIS R1655(ファインセラミックスの水銀圧入法による成形体気孔径分布試験方法)に準拠して測定した全細孔容積(単位:cm3/g)と、ガス置換式密度測定計(マイクロメリティックス社製、アキュピック1330)により測定した見掛け密度(単位:g/cm3)を用いて、下記式(2)より算出した。
式2:気孔率[%]=全細孔容積/{(1/見掛け密度)+全細孔容積} ×100
式2:気孔率[%]=全細孔容積/{(1/見掛け密度)+全細孔容積} ×100
熱膨張係数は、上記した原料スラリーを3mm×4mm×20mmのバルク体に成形した後、バルク体を800℃で焼成して測定用試料を作製した。その後、測定用試料を、熱膨張計を用いてJIS R1618(ファインセラミックスの熱機械分析による熱膨張の測定方法)に準拠して測定した。なお、熱膨張係数の測定は、多孔質保護層と金属板を別個に測定した。
また、試料1~4の多孔質保護層、及び、試料1~12の金属板について、熱伝導率の測定を行った。熱伝導率も、多孔質保護層と金属板を別個に測定した。熱伝導率は、熱拡散率、比熱容量及び嵩密度を乗算し、算出した。熱拡散率は、レーザーフラッシュ法熱定数測定装置を用い、比熱容量はDSC(示差走査熱量計)を用いて、JIS R1611(ファインセラミックスのレーザーフラッシュ法による熱拡散率・比熱容量・熱伝導率試験方法)に準拠して室温で測定した。金属板の嵩密度は、φ10mm×厚み1mmのバルク体の重量を測定し、その重量を体積で割った値を嵩密度(単位:g/cm3)とした。また、多孔質保護層の嵩密度(単位:cm3/g)は下記式(3)から算出した。なお、熱拡散率は上記した原料スラリーをφ10mm×厚み1mmのバルク体に成形し、また、比熱容量は上記した原料スラリーをφ5mm×厚み1mmのバルク体に成形した後、それぞれのバルク体を800℃で焼成して熱拡散率および比熱容量測定用試料を作製し、測定した。測定結果を図15に示す。
式3:多孔質保護層の嵩密度=見掛け密度×(1-気孔率[%]/100)
式3:多孔質保護層の嵩密度=見掛け密度×(1-気孔率[%]/100)
図15に示すように、試料1~10は、焼成後の多孔質保護層にクラック及び剥離が確認されなかった。一方、試料11は、剥離は確認されなかったもののクラックの発生が確認された。また、試料12は、クラックと剥離の両方が確認された。この結果は、多孔質保護層内のアルミナ成分(アルミナ繊維及び板状アルミナ粒子)が少ない(15質量%未満)、又は、チタニア成分が少ない(45質量%未満)場合、焼成の際に金属-多孔質保護層間に力が作用し、多孔質保護層の特性が低下することを示している。具体的には、試料11は、アルミナ成分の割合が15質量%未満であるため、セラミックス(粒子、繊維)間の結合力が低下し、多孔質保護層にクラックが発生したと推察される。また、試料12は、チタニア成分の割合が45質量%未満であるため、セラミックス間の結合力が低下し、多孔質保護層にクラックが発生したと推察される。さらに試料12は、熱膨張係数が高いチタニア成分(チタニア粒子)の含有率が低く、金属に対する熱膨張係数比(α1/α2)が小さいので(0.5未満)、金属と多孔質保護層間の熱膨張差に基づいて多孔質保護層が金属から剥離したと推察される。以上より、15質量%以上のアルミナ成分と45質量%以上のチタニア成分を含む多孔質保護層は、焼成後にクラック及び剥離等の劣化が生じにくくなることが確認された。
以上、本発明の実施形態について詳細に説明したが、これらは例示に過ぎず、請求の範囲を限定するものではない。請求の範囲に記載の技術には、以上に例示した具体例を様々に変形、変更したものが含まれる。また、本明細書または図面に説明した技術要素は、単独であるいは各種の組合せによって技術的有用性を発揮するものであり、出願時請求項記載の組合せに限定されるものではない。また、本明細書または図面に例示した技術は複数目的を同時に達成するものであり、そのうちの一つの目的を達成すること自体で技術的有用性を持つものである。
Claims (12)
- 金属の表面に無機多孔質層が設けられている複合部材であって、
無機多孔質層は、
セラミック繊維を含み、
15質量%以上のアルミナ成分と45質量%以上のチタニア成分によって構成されている、複合部材。 - 前記金属の熱伝導率が、無機多孔質層の熱伝導率の100倍以上である請求項1に記載の複合部材。
- 無機多孔質層の熱伝導率が、0.05W/mK以上3W/mK以下である請求項2に記載の複合部材。
- 前記金属の熱伝導率が、10W/mK以上400W/mK以下である請求項2または3に記載の複合部材。
- 無機多孔質層の熱膨張係数をα1とし、前記金属の熱膨張係数をα2としたときに、下記式(1)を満足する請求項1から4のいずれか一項に記載の複合部材。
0.5<α1/α2<1.2 (1) - 無機多孔質層に、板状セラミックス粒子が含まれている請求項1から5のいずれか一項に記載の複合部材。
- 無機多孔質層に、0.1μm以上10μm以下の粒状粒子が含まれている請求項1から6のいずれか一項に記載の複合部材。
- 無機多孔質層の厚みが1mm以上である請求項1から7のいずれか一項に記載の複合部材。
- 前記金属が板状である請求項1から8のいずれか一項に記載の複合部材。
- 前記金属が管状である請求項1から8のいずれか一項に記載の複合部材。
- 前記金属が線状である請求項1から8のいずれか一項に記載の複合部材。
- 無機多孔質層の前記金属が設けられている面とは反対側の面に、被覆層が設けられている請求項1から11のいずれか一項に記載の複合部材。
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2020536833A JP6813718B2 (ja) | 2019-01-10 | 2020-01-09 | 複合部材 |
| DE112020000388.4T DE112020000388T5 (de) | 2019-01-10 | 2020-01-09 | Verbundelement |
| CN202080008375.6A CN113272475B (zh) | 2019-01-10 | 2020-01-09 | 复合部件 |
| US17/305,410 US20210331450A1 (en) | 2019-01-10 | 2021-07-07 | Composite member |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JPPCT/JP2019/000585 | 2019-01-10 | ||
| JP2019000585 | 2019-01-10 | ||
| JP2019-182462 | 2019-10-02 | ||
| JP2019182462 | 2019-10-02 |
Related Child Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| US17/305,410 Continuation US20210331450A1 (en) | 2019-01-10 | 2021-07-07 | Composite member |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2020145366A1 true WO2020145366A1 (ja) | 2020-07-16 |
Family
ID=71520965
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2020/000540 Ceased WO2020145365A1 (ja) | 2019-01-10 | 2020-01-09 | 放熱部材 |
| PCT/JP2020/000541 Ceased WO2020145366A1 (ja) | 2019-01-10 | 2020-01-09 | 複合部材 |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2020/000540 Ceased WO2020145365A1 (ja) | 2019-01-10 | 2020-01-09 | 放熱部材 |
Country Status (5)
| Country | Link |
|---|---|
| US (2) | US20210341234A1 (ja) |
| JP (3) | JP6813718B2 (ja) |
| CN (2) | CN113272474A (ja) |
| DE (2) | DE112020000384T5 (ja) |
| WO (2) | WO2020145365A1 (ja) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2022014617A1 (ja) * | 2020-07-13 | 2022-01-20 | 日本碍子株式会社 | 排気管 |
| WO2022014611A1 (ja) * | 2020-07-13 | 2022-01-20 | 日本碍子株式会社 | 複合部材 |
| WO2022014616A1 (ja) * | 2020-07-13 | 2022-01-20 | 日本碍子株式会社 | 排気管 |
| WO2022014615A1 (ja) * | 2020-07-13 | 2022-01-20 | 日本碍子株式会社 | 排気管 |
| JP2022170754A (ja) * | 2021-04-29 | 2022-11-11 | 日本特殊陶業株式会社 | セラミックス多孔体 |
| JP2023075698A (ja) * | 2021-11-19 | 2023-05-31 | 国立研究開発法人宇宙航空研究開発機構 | ホローカソード |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP7796396B2 (ja) * | 2020-11-26 | 2026-01-09 | 国立研究開発法人産業技術総合研究所 | 複合体及びその製造方法 |
| CN116061513A (zh) * | 2023-01-10 | 2023-05-05 | 扬州金鑫管业有限公司 | 一种耐锈蚀陶瓷复合金属材料及其生产工艺 |
| TWI901138B (zh) * | 2024-05-22 | 2025-10-11 | 世銓科技股份有限公司 | 熱擴散器件及其多孔隙載體 |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH08319582A (ja) * | 1995-05-19 | 1996-12-03 | Isuzu Ceramics Kenkyusho:Kk | 金属表面の絶縁性セラミックス膜及びその形成方法 |
| JPH0941116A (ja) * | 1995-07-28 | 1997-02-10 | Toshiba Corp | 耐熱部材およびその製造方法 |
| JP2009536982A (ja) * | 2006-01-25 | 2009-10-22 | セラマテック・インク | 予備被覆基板を保護するための環境および熱バリア皮膜 |
| JP2010188299A (ja) * | 2009-02-19 | 2010-09-02 | Nippon Electric Glass Co Ltd | 白金材料容器の乾燥被膜及び焼成被膜の形成方法 |
| WO2013081150A1 (ja) * | 2011-12-02 | 2013-06-06 | 日本碍子株式会社 | エンジン燃焼室構造、および流路の内壁構造 |
| JP2017214913A (ja) * | 2016-06-02 | 2017-12-07 | 株式会社東芝 | 蒸気タービン翼及びその製造方法 |
Family Cites Families (42)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1436842A (en) * | 1972-06-08 | 1976-05-26 | Tennant & Sons Warrington Ltd | Radiant gas-fired burner |
| GB1580909A (en) * | 1977-02-10 | 1980-12-10 | Micropore Internatioonal Ltd | Thermal insulation material |
| US4639388A (en) * | 1985-02-12 | 1987-01-27 | Chromalloy American Corporation | Ceramic-metal composites |
| US4921731A (en) * | 1986-02-25 | 1990-05-01 | University Of Florida | Deposition of ceramic coatings using sol-gel processing with application of a thermal gradient |
| DE3741732C1 (de) * | 1987-12-09 | 1988-12-22 | Messerschmitt Boelkow Blohm | Mehrschicht-Waermedaemmung |
| US5667898A (en) * | 1989-01-30 | 1997-09-16 | Lanxide Technology Company, Lp | Self-supporting aluminum titanate composites and products relating thereto |
| JPH03153092A (ja) * | 1989-11-10 | 1991-07-01 | Mitsubishi Heavy Ind Ltd | 電子基板 |
| JPH07216479A (ja) * | 1994-01-31 | 1995-08-15 | Ee M Technol:Kk | 金属複合体 |
| US5585136A (en) * | 1995-03-22 | 1996-12-17 | Queen's University At Kingston | Method for producing thick ceramic films by a sol gel coating process |
| DE19542944C2 (de) * | 1995-11-17 | 1998-01-22 | Daimler Benz Ag | Brennkraftmaschine und Verfahren zum Aufbringen einer Wärmedämmschicht |
| US6849334B2 (en) * | 2001-08-17 | 2005-02-01 | Neophotonics Corporation | Optical materials and optical devices |
| JPH11216795A (ja) * | 1998-01-30 | 1999-08-10 | Dainippon Printing Co Ltd | 外装用断熱シート及び外装用化粧材 |
| US6733907B2 (en) * | 1998-03-27 | 2004-05-11 | Siemens Westinghouse Power Corporation | Hybrid ceramic material composed of insulating and structural ceramic layers |
| US8357454B2 (en) * | 2001-08-02 | 2013-01-22 | Siemens Energy, Inc. | Segmented thermal barrier coating |
| US20070163250A1 (en) * | 2004-03-03 | 2007-07-19 | Sane Ajit Y | Highly insulated exhaust manifold |
| JP4903457B2 (ja) * | 2005-09-06 | 2012-03-28 | 財団法人電力中央研究所 | 金属−多孔質基材複合材料及びその製造方法 |
| JP4679324B2 (ja) * | 2005-09-30 | 2011-04-27 | イビデン株式会社 | 断熱材 |
| US7628951B1 (en) * | 2005-10-21 | 2009-12-08 | Ceramatec, Inc. | Process for making ceramic insulation |
| JP2007230858A (ja) * | 2006-02-02 | 2007-09-13 | Nichias Corp | 断熱材及びその製造方法 |
| JP5014656B2 (ja) * | 2006-03-27 | 2012-08-29 | 国立大学法人東北大学 | プラズマ処理装置用部材およびその製造方法 |
| DE102006038713A1 (de) * | 2006-05-10 | 2007-11-29 | Schunk Kohlenstofftechnik Gmbh | Druckfester fluidbeaufschlagter Körper |
| US7855163B2 (en) * | 2007-05-14 | 2010-12-21 | Geo2 Technologies, Inc. | Low coefficient of thermal expansion bonding system for a high porosity ceramic body and methods of manufacture |
| JP2010024077A (ja) * | 2008-07-17 | 2010-02-04 | Denki Kagaku Kogyo Kk | アルミニウム−炭化珪素質複合体及びその製造方法 |
| JP2010050239A (ja) * | 2008-08-21 | 2010-03-04 | Hitachi Ltd | 放熱シート、それを用いた放熱用積層板及び半導体装置 |
| JP4962510B2 (ja) * | 2009-02-25 | 2012-06-27 | 日本電気株式会社 | 目標捜索信号生成方法および目標捜索装置 |
| CN102740947A (zh) * | 2009-12-21 | 2012-10-17 | 美商绩优图科技股份有限公司 | 经纤维强化的多孔性基材 |
| JP2012119671A (ja) * | 2010-11-11 | 2012-06-21 | Kitagawa Ind Co Ltd | 電子回路及びヒートシンク |
| JP5727808B2 (ja) * | 2011-02-09 | 2015-06-03 | イビデン株式会社 | 構造体、及び、構造体の製造方法 |
| JP5764506B2 (ja) * | 2012-02-08 | 2015-08-19 | 美濃窯業株式会社 | セラミックス多孔体−金属断熱材及びその製造方法 |
| JP5390682B1 (ja) * | 2012-11-13 | 2014-01-15 | 日本特殊陶業株式会社 | ガスセンサ素子及びガスセンサ |
| JP2015116697A (ja) * | 2013-12-17 | 2015-06-25 | Jsr株式会社 | 塗装体 |
| JP6220296B2 (ja) * | 2014-03-19 | 2017-10-25 | 日本碍子株式会社 | 耐熱性部材及びその製造方法 |
| JP6839981B2 (ja) * | 2014-07-24 | 2021-03-10 | デンカ株式会社 | 複合体及びその製造方法 |
| EP3297971B1 (de) * | 2015-05-19 | 2022-03-16 | Basf Se | Gasdichtes, mehrschichtiges verbundrohr |
| JP6207682B2 (ja) * | 2015-07-06 | 2017-10-04 | 日本碍子株式会社 | 積層体及び電気化学デバイス |
| JP6716296B2 (ja) * | 2016-03-11 | 2020-07-01 | 日本特殊陶業株式会社 | 多孔体複合部材 |
| CN109219588A (zh) * | 2016-06-24 | 2019-01-15 | 巴斯夫欧洲公司 | 敞口容器及其用途 |
| JP6743579B2 (ja) * | 2016-08-24 | 2020-08-19 | 船井電機株式会社 | 受電装置 |
| FR3058469B1 (fr) * | 2016-11-09 | 2020-08-21 | Safran | Piece de turbomachine revetue d'une barriere thermique et procede pour l'obtenir |
| EP3575366A4 (en) * | 2017-01-19 | 2020-10-28 | University of Fukui | MATERIAL WITH HIGH THERMAL CONDUCTIVITY AND ITS PRODUCTION PROCESS |
| JP2018184860A (ja) * | 2017-04-25 | 2018-11-22 | 日立オートモティブシステムズ株式会社 | 内燃機関のピストン及び内燃機関のピストン冷却制御方法 |
| CN107326330B (zh) * | 2017-06-30 | 2019-03-12 | 福州大学 | 一种具有氧化铝多孔结构缓冲层的内热式一体化蒸发舟 |
-
2020
- 2020-01-09 WO PCT/JP2020/000540 patent/WO2020145365A1/ja not_active Ceased
- 2020-01-09 JP JP2020536833A patent/JP6813718B2/ja active Active
- 2020-01-09 DE DE112020000384.1T patent/DE112020000384T5/de active Pending
- 2020-01-09 JP JP2020565215A patent/JP7431176B2/ja active Active
- 2020-01-09 DE DE112020000388.4T patent/DE112020000388T5/de active Pending
- 2020-01-09 CN CN202080008368.6A patent/CN113272474A/zh active Pending
- 2020-01-09 CN CN202080008375.6A patent/CN113272475B/zh active Active
- 2020-01-09 WO PCT/JP2020/000541 patent/WO2020145366A1/ja not_active Ceased
- 2020-12-18 JP JP2020210574A patent/JP7423502B2/ja active Active
-
2021
- 2021-07-07 US US17/305,409 patent/US20210341234A1/en not_active Abandoned
- 2021-07-07 US US17/305,410 patent/US20210331450A1/en not_active Abandoned
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH08319582A (ja) * | 1995-05-19 | 1996-12-03 | Isuzu Ceramics Kenkyusho:Kk | 金属表面の絶縁性セラミックス膜及びその形成方法 |
| JPH0941116A (ja) * | 1995-07-28 | 1997-02-10 | Toshiba Corp | 耐熱部材およびその製造方法 |
| JP2009536982A (ja) * | 2006-01-25 | 2009-10-22 | セラマテック・インク | 予備被覆基板を保護するための環境および熱バリア皮膜 |
| JP2010188299A (ja) * | 2009-02-19 | 2010-09-02 | Nippon Electric Glass Co Ltd | 白金材料容器の乾燥被膜及び焼成被膜の形成方法 |
| WO2013081150A1 (ja) * | 2011-12-02 | 2013-06-06 | 日本碍子株式会社 | エンジン燃焼室構造、および流路の内壁構造 |
| JP2017214913A (ja) * | 2016-06-02 | 2017-12-07 | 株式会社東芝 | 蒸気タービン翼及びその製造方法 |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2022014617A1 (ja) * | 2020-07-13 | 2022-01-20 | 日本碍子株式会社 | 排気管 |
| WO2022014611A1 (ja) * | 2020-07-13 | 2022-01-20 | 日本碍子株式会社 | 複合部材 |
| WO2022014616A1 (ja) * | 2020-07-13 | 2022-01-20 | 日本碍子株式会社 | 排気管 |
| WO2022014615A1 (ja) * | 2020-07-13 | 2022-01-20 | 日本碍子株式会社 | 排気管 |
| JP2022170754A (ja) * | 2021-04-29 | 2022-11-11 | 日本特殊陶業株式会社 | セラミックス多孔体 |
| JP7610465B2 (ja) | 2021-04-29 | 2025-01-08 | 日本特殊陶業株式会社 | セラミックス多孔体 |
| JP2023075698A (ja) * | 2021-11-19 | 2023-05-31 | 国立研究開発法人宇宙航空研究開発機構 | ホローカソード |
| JP7756356B2 (ja) | 2021-11-19 | 2025-10-20 | 国立研究開発法人宇宙航空研究開発機構 | ホローカソード |
Also Published As
| Publication number | Publication date |
|---|---|
| JP6813718B2 (ja) | 2021-01-13 |
| DE112020000388T5 (de) | 2021-09-23 |
| JP7423502B2 (ja) | 2024-01-29 |
| CN113272475B (zh) | 2023-06-27 |
| US20210331450A1 (en) | 2021-10-28 |
| US20210341234A1 (en) | 2021-11-04 |
| JP7431176B2 (ja) | 2024-02-14 |
| JPWO2020145365A1 (ja) | 2021-11-25 |
| CN113272475A (zh) | 2021-08-17 |
| WO2020145365A1 (ja) | 2020-07-16 |
| DE112020000384T5 (de) | 2021-09-23 |
| JP2021054088A (ja) | 2021-04-08 |
| JPWO2020145366A1 (ja) | 2021-02-18 |
| CN113272474A (zh) | 2021-08-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP7423502B2 (ja) | 複合部材 | |
| US7651755B2 (en) | Honeycomb structure and seal material | |
| EP2865722B1 (en) | Porous plate-shaped filler, coating composition, heat-insulating film, and heat-insulating film structure | |
| US9028946B2 (en) | Ceramic honeycomb structure with applied inorganic skin | |
| US12153012B2 (en) | Gas sensor | |
| US20220252540A1 (en) | Sensor element | |
| JP7178420B2 (ja) | セラミックス構造体およびガスセンサのセンサ素子 | |
| WO2022014613A1 (ja) | 排気管 | |
| WO2020067318A1 (ja) | セラミックス構造体およびガスセンサのセンサ素子 | |
| WO2022014611A1 (ja) | 複合部材 | |
| JP2022017128A (ja) | 複合部材 | |
| WO2022014614A1 (ja) | 排気管 | |
| CN110118813B (zh) | 气体传感器元件 | |
| WO2022014612A1 (ja) | 排気管 | |
| JP7743345B2 (ja) | 排気管 | |
| WO2022014617A1 (ja) | 排気管 | |
| WO2022014616A1 (ja) | 排気管 | |
| WO2022014615A1 (ja) | 排気管 | |
| JP2022149955A (ja) | 複合焼結体、ハニカム構造体、電気加熱触媒および複合焼結体の製造方法 | |
| JP4107990B2 (ja) | 電気化学素子 | |
| JP2023128877A (ja) | 複合焼結体、ハニカム構造体、電気加熱触媒および複合焼結体の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| ENP | Entry into the national phase |
Ref document number: 2020536833 Country of ref document: JP Kind code of ref document: A |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 20738554 Country of ref document: EP Kind code of ref document: A1 |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 20738554 Country of ref document: EP Kind code of ref document: A1 |