EP0982124B1 - Verfahren zur Herstellung von Hochdruckplatten durch Gravur-Aufzeichnung mittels kohärenter elektromagnetischer Strahlung und damit hergestellte Druckplatte - Google Patents
Verfahren zur Herstellung von Hochdruckplatten durch Gravur-Aufzeichnung mittels kohärenter elektromagnetischer Strahlung und damit hergestellte Druckplatte Download PDFInfo
- Publication number
- EP0982124B1 EP0982124B1 EP99116468A EP99116468A EP0982124B1 EP 0982124 B1 EP0982124 B1 EP 0982124B1 EP 99116468 A EP99116468 A EP 99116468A EP 99116468 A EP99116468 A EP 99116468A EP 0982124 B1 EP0982124 B1 EP 0982124B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- filler
- laser
- engraving
- layer
- polymeric
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000007639 printing Methods 0.000 title claims description 32
- 238000000034 method Methods 0.000 title claims description 22
- 230000008569 process Effects 0.000 title claims description 17
- 230000001427 coherent effect Effects 0.000 title claims description 8
- 230000005670 electromagnetic radiation Effects 0.000 title claims description 8
- 239000000463 material Substances 0.000 claims description 40
- 239000000945 filler Substances 0.000 claims description 22
- 229920002451 polyvinyl alcohol Polymers 0.000 claims description 19
- 239000004372 Polyvinyl alcohol Substances 0.000 claims description 18
- 229920003229 poly(methyl methacrylate) Polymers 0.000 claims description 17
- 229920000642 polymer Polymers 0.000 claims description 17
- -1 poly(ethylene) Polymers 0.000 claims description 16
- 229920006324 polyoxymethylene Polymers 0.000 claims description 15
- 229930040373 Paraformaldehyde Natural products 0.000 claims description 13
- 239000011230 binding agent Substances 0.000 claims description 12
- 229920001577 copolymer Polymers 0.000 claims description 9
- 239000002245 particle Substances 0.000 claims description 9
- 150000001875 compounds Chemical class 0.000 claims description 8
- 239000011324 bead Substances 0.000 claims description 6
- 239000004926 polymethyl methacrylate Substances 0.000 claims description 6
- 229910052700 potassium Inorganic materials 0.000 claims description 6
- 230000005855 radiation Effects 0.000 claims description 6
- 239000007787 solid Substances 0.000 claims description 6
- 239000004793 Polystyrene Substances 0.000 claims description 4
- 230000007062 hydrolysis Effects 0.000 claims description 4
- 238000006460 hydrolysis reaction Methods 0.000 claims description 4
- 229920002223 polystyrene Polymers 0.000 claims description 4
- 238000010894 electron beam technology Methods 0.000 claims description 3
- 150000002576 ketones Chemical class 0.000 claims description 3
- 239000004014 plasticizer Substances 0.000 claims description 3
- 229920003251 poly(α-methylstyrene) Polymers 0.000 claims description 3
- 239000000654 additive Substances 0.000 claims description 2
- 238000004132 cross linking Methods 0.000 claims description 2
- 239000003505 polymerization initiator Substances 0.000 claims description 2
- 239000003381 stabilizer Substances 0.000 claims description 2
- 239000003086 colorant Substances 0.000 claims 1
- 238000007644 letterpress printing Methods 0.000 claims 1
- 239000000758 substrate Substances 0.000 claims 1
- 239000010410 layer Substances 0.000 description 32
- 235000019422 polyvinyl alcohol Nutrition 0.000 description 18
- 238000004519 manufacturing process Methods 0.000 description 17
- 238000010147 laser engraving Methods 0.000 description 12
- 239000010408 film Substances 0.000 description 10
- LYCAIKOWRPUZTN-UHFFFAOYSA-N Ethylene glycol Chemical compound OCCO LYCAIKOWRPUZTN-UHFFFAOYSA-N 0.000 description 9
- 238000001035 drying Methods 0.000 description 9
- 239000000203 mixture Substances 0.000 description 8
- 239000003999 initiator Substances 0.000 description 7
- 239000012456 homogeneous solution Substances 0.000 description 6
- BDERNNFJNOPAEC-UHFFFAOYSA-N propan-1-ol Chemical compound CCCO BDERNNFJNOPAEC-UHFFFAOYSA-N 0.000 description 6
- OARRHUQTFTUEOS-UHFFFAOYSA-N safranin Chemical compound [Cl-].C=12C=C(N)C(C)=CC2=NC2=CC(C)=C(N)C=C2[N+]=1C1=CC=CC=C1 OARRHUQTFTUEOS-UHFFFAOYSA-N 0.000 description 6
- 239000011243 crosslinked material Substances 0.000 description 5
- 239000000975 dye Substances 0.000 description 5
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 5
- KWVGIHKZDCUPEU-UHFFFAOYSA-N 2,2-dimethoxy-2-phenylacetophenone Chemical compound C=1C=CC=CC=1C(OC)(OC)C(=O)C1=CC=CC=C1 KWVGIHKZDCUPEU-UHFFFAOYSA-N 0.000 description 3
- 229920002799 BoPET Polymers 0.000 description 3
- IMROMDMJAWUWLK-UHFFFAOYSA-N Ethenol Chemical compound OC=C IMROMDMJAWUWLK-UHFFFAOYSA-N 0.000 description 3
- OKKJLVBELUTLKV-UHFFFAOYSA-N Methanol Chemical compound OC OKKJLVBELUTLKV-UHFFFAOYSA-N 0.000 description 3
- 229910052782 aluminium Inorganic materials 0.000 description 3
- 230000008901 benefit Effects 0.000 description 3
- 230000000052 comparative effect Effects 0.000 description 3
- 239000004814 polyurethane Substances 0.000 description 3
- XAEFZNCEHLXOMS-UHFFFAOYSA-M potassium benzoate Chemical compound [K+].[O-]C(=O)C1=CC=CC=C1 XAEFZNCEHLXOMS-UHFFFAOYSA-M 0.000 description 3
- 239000012744 reinforcing agent Substances 0.000 description 3
- 238000001878 scanning electron micrograph Methods 0.000 description 3
- 239000002356 single layer Substances 0.000 description 3
- NIXOWILDQLNWCW-UHFFFAOYSA-M Acrylate Chemical compound [O-]C(=O)C=C NIXOWILDQLNWCW-UHFFFAOYSA-M 0.000 description 2
- LFQSCWFLJHTTHZ-UHFFFAOYSA-N Ethanol Chemical compound CCO LFQSCWFLJHTTHZ-UHFFFAOYSA-N 0.000 description 2
- 229920005027 Ultraform® Polymers 0.000 description 2
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 2
- 238000006243 chemical reaction Methods 0.000 description 2
- 239000011248 coating agent Substances 0.000 description 2
- 238000000576 coating method Methods 0.000 description 2
- 239000013039 cover film Substances 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 229920001600 hydrophobic polymer Polymers 0.000 description 2
- 239000003112 inhibitor Substances 0.000 description 2
- LXCJGJYAOVCKLO-UHFFFAOYSA-N n-cyclohexyl-n-hydroxynitrous amide Chemical compound O=NN(O)C1CCCCC1 LXCJGJYAOVCKLO-UHFFFAOYSA-N 0.000 description 2
- 230000006855 networking Effects 0.000 description 2
- 229920000728 polyester Polymers 0.000 description 2
- 238000006116 polymerization reaction Methods 0.000 description 2
- 229920002635 polyurethane Polymers 0.000 description 2
- 229920002689 polyvinyl acetate Polymers 0.000 description 2
- 239000011118 polyvinyl acetate Substances 0.000 description 2
- 239000011877 solvent mixture Substances 0.000 description 2
- 239000007858 starting material Substances 0.000 description 2
- 238000012360 testing method Methods 0.000 description 2
- 238000012546 transfer Methods 0.000 description 2
- 229920001567 vinyl ester resin Polymers 0.000 description 2
- YKHNTDZZKRMCQV-UHFFFAOYSA-N 2-(phenoxymethyl)oxirane;prop-2-enoic acid Chemical compound OC(=O)C=C.C1OC1COC1=CC=CC=C1 YKHNTDZZKRMCQV-UHFFFAOYSA-N 0.000 description 1
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 1
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 1
- 229920000742 Cotton Polymers 0.000 description 1
- UDOKVFSRUXCTGS-UHFFFAOYSA-N N-[1,2-dihydroxy-2-[hydroxymethyl(prop-2-enoyl)amino]ethyl]-N-(hydroxymethyl)prop-2-enamide Chemical compound C(O)N(C(C=C)=O)C(C(N(C(C=C)=O)CO)O)O UDOKVFSRUXCTGS-UHFFFAOYSA-N 0.000 description 1
- 239000004677 Nylon Substances 0.000 description 1
- 229920002266 Pluriol® Polymers 0.000 description 1
- 239000004952 Polyamide Substances 0.000 description 1
- 239000002202 Polyethylene glycol Substances 0.000 description 1
- 229920000297 Rayon Polymers 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 description 1
- 238000002679 ablation Methods 0.000 description 1
- 239000011358 absorbing material Substances 0.000 description 1
- 150000001298 alcohols Chemical class 0.000 description 1
- 239000000783 alginic acid Substances 0.000 description 1
- 230000003321 amplification Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000005540 biological transmission Effects 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000006229 carbon black Substances 0.000 description 1
- 239000001913 cellulose Substances 0.000 description 1
- 229920002678 cellulose Polymers 0.000 description 1
- 229920002301 cellulose acetate Polymers 0.000 description 1
- 239000003795 chemical substances by application Substances 0.000 description 1
- 229910052802 copper Inorganic materials 0.000 description 1
- 239000010949 copper Substances 0.000 description 1
- JGDFBJMWFLXCLJ-UHFFFAOYSA-N copper chromite Chemical compound [Cu]=O.[Cu]=O.O=[Cr]O[Cr]=O JGDFBJMWFLXCLJ-UHFFFAOYSA-N 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 239000003599 detergent Substances 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 238000011982 device technology Methods 0.000 description 1
- QDOXWKRWXJOMAK-UHFFFAOYSA-N dichromium trioxide Chemical compound O=[Cr]O[Cr]=O QDOXWKRWXJOMAK-UHFFFAOYSA-N 0.000 description 1
- 239000006185 dispersion Substances 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 229920001971 elastomer Polymers 0.000 description 1
- 239000000806 elastomer Substances 0.000 description 1
- 239000000839 emulsion Substances 0.000 description 1
- RTZKZFJDLAIYFH-UHFFFAOYSA-N ether Substances CCOCC RTZKZFJDLAIYFH-UHFFFAOYSA-N 0.000 description 1
- 238000001125 extrusion Methods 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 239000011888 foil Substances 0.000 description 1
- 230000009477 glass transition Effects 0.000 description 1
- 239000011491 glass wool Substances 0.000 description 1
- 229920000578 graft copolymer Polymers 0.000 description 1
- 239000008187 granular material Substances 0.000 description 1
- 229910002804 graphite Inorganic materials 0.000 description 1
- 239000010439 graphite Substances 0.000 description 1
- 229920001519 homopolymer Polymers 0.000 description 1
- 239000001023 inorganic pigment Substances 0.000 description 1
- 229920002521 macromolecule Polymers 0.000 description 1
- 239000000155 melt Substances 0.000 description 1
- 239000002923 metal particle Substances 0.000 description 1
- VNWKTOKETHGBQD-UHFFFAOYSA-N methane Chemical compound C VNWKTOKETHGBQD-UHFFFAOYSA-N 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 239000000178 monomer Substances 0.000 description 1
- 238000003199 nucleic acid amplification method Methods 0.000 description 1
- 229920001778 nylon Polymers 0.000 description 1
- 238000004806 packaging method and process Methods 0.000 description 1
- 239000000123 paper Substances 0.000 description 1
- 239000000049 pigment Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 229920002239 polyacrylonitrile Polymers 0.000 description 1
- 229920002647 polyamide Polymers 0.000 description 1
- 238000006068 polycondensation reaction Methods 0.000 description 1
- 229920001223 polyethylene glycol Polymers 0.000 description 1
- 239000002952 polymeric resin Substances 0.000 description 1
- 229920000909 polytetrahydrofuran Polymers 0.000 description 1
- 229920000915 polyvinyl chloride Polymers 0.000 description 1
- 230000002787 reinforcement Effects 0.000 description 1
- 230000003014 reinforcing effect Effects 0.000 description 1
- 230000004044 response Effects 0.000 description 1
- 238000007650 screen-printing Methods 0.000 description 1
- 150000003384 small molecules Chemical class 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
- 238000005406 washing Methods 0.000 description 1
- 229910052725 zinc Inorganic materials 0.000 description 1
- 239000011701 zinc Substances 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41C—PROCESSES FOR THE MANUFACTURE OR REPRODUCTION OF PRINTING SURFACES
- B41C1/00—Forme preparation
- B41C1/02—Engraving; Heads therefor
- B41C1/04—Engraving; Heads therefor using heads controlled by an electric information signal
- B41C1/05—Heat-generating engraving heads, e.g. laser beam, electron beam
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10S—TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10S430/00—Radiation imagery chemistry: process, composition, or product thereof
- Y10S430/1053—Imaging affecting physical property or radiation sensitive material, or producing nonplanar or printing surface - process, composition, or product: radiation sensitive composition or product or process of making binder containing
- Y10S430/1055—Radiation sensitive composition or product or process of making
- Y10S430/106—Binder containing
- Y10S430/11—Vinyl alcohol polymer or derivative
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10S—TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10S430/00—Radiation imagery chemistry: process, composition, or product thereof
- Y10S430/1053—Imaging affecting physical property or radiation sensitive material, or producing nonplanar or printing surface - process, composition, or product: radiation sensitive composition or product or process of making binder containing
- Y10S430/1055—Radiation sensitive composition or product or process of making
- Y10S430/114—Initiator containing
Definitions
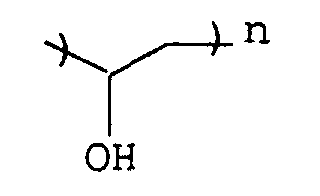
- the invention relates to a material for engraving recording by means of coherent electromagnetic radiation, consisting of carrier, crosslinkable layer, optionally a cover layer, optionally a cover film, the crosslinkable layer containing at least one ethylenically unsaturated compound and a polymerization initiator and at least one polymeric binder , which consists of a polyvinyl alcohol with a degree of hydrolysis of 50-99% and / or one or more copolymers, which make up a significant proportion of the structural unit exhibit.
- Such materials are for printing forms for high pressure known.
- WO 93/23252 describes a method for laser engraving an elastomer Single-layer flexographic printing plate described, wherein a mechanical, photochemical or thermochemical amplification of the Single layer material and engraving with a selected pattern should take place for the production of the finished engraved flexographic printing plate.
- the single-layer material contains reinforcing agents the mechanically and / or thermochemically and / or photochemically should work. Such reinforcing agents are advantageous for rubber-like flexo materials to improve the engraving in the With regard to a higher image resolution for packaging printing.
- Radiation absorbing materials can be used as mechanical reinforcing means Pigments serve e.g.
- finely divided metal particles such as aluminum, copper or zinc, alone or in combination with Carbon black, graphite, copper chromite, chrome oxide, cobalt-chrome-aluminum and other dark, inorganic pigments.
- various fibers synthetic or natural, e.g. Cellulose, cotton, cellulose acetate, Viscose, paper, glass wool, nylon and polyester.
- Such mechanical reinforcement means are for crosslinkable PVA binders cannot be used for high-pressure plates.
- the CO 2 laser Due to the high energy input and its reliability, the CO 2 laser enables a good material removal rate during the engraving process.
- EP-A 767 406 is an IR laser method for ablation an IR-sensitive layer for the production of a mask for known imagewise UV exposure of a high pressure plate.
- a Such mask production differs in principle from an engraving of a printing plate.
- JP-A 6 230 568 discloses a photosensitive composition for the production of high-pressure and screen printing plates.
- the Composition comprises an emulsion of a hydrophobic polymer resin with a glass transition temperature> 45 ° C, a polymer of Polyvinyl alcohol type, photopolymerizable monomers and one Photopolymerization initiator.
- the hydrophobic polymer can it is for example PVC, polyacrylonitrile, polystyrene or Act PMMA.
- the script describes conventional production a high pressure plate using this composition by covering the photosensitive layer with a photographic Negative, exposure of the layer to UV light through the negative followed by developing the exposed layer using a detergent. The possibility of engraving a Print reliefs with a laser are not disclosed.
- the object of the present invention is a method to provide for the production of high-pressure plates, at which by means of coherent electromagnetic radiation records or printed products with high resolution in a short time can be.
- the object is achieved with a method for engraving recording using coherent electromagnetic radiation, using a material consisting of a support, a crosslinkable layer, optionally a cover layer, optionally a cover film, and the crosslinkable layer at least one ethylenically unsaturated compound and a polymerization.
- Initiator and at least one polymeric binder which consists of a polyvinyl alcohol with a degree of hydrolysis of 50 to 99% and / or one or more copolymers, the structural unit in a significant proportion have, and also a polymer filler is provided which has a ceiling temperature of less than 800 K, in particular less than 600 K.
- Croiling temperature is the temperature at which the depolymerization of a macromolecule from the chain end begins.
- the particular advantage of using the filler with a predetermined Ceiling temperature limit is that the material for the high pressure is surprisingly usable and the Engraving speed can increase significantly without it Loss in print quality comes.
- the filler can be crosslinked or can be cross-linked or non-cross-linked, the filler can be expedient one or more of the following polymers:
- PS Polystyrene
- PMMA polymethyl methacrylate
- POM polyoxymethylene
- POM polytetrahydrofuran
- poly ( ⁇ -methylstyrene) polystyrene
- the filler in particle form in particular spherical or Approximately spherical in shape, the largest dimension being about 5-10 ⁇ m is.
- the polymeric filler can be coated with a Weight percentage from 1 to 49.9%, in particular from 2 to 25%, preferably 5-15%, based on the solids of the crosslinkable layer B) can be used.
- the polymeric filler has a ceiling temperature of less than 500 K and in particular from polymethyl methacrylate (PMMA) or from polyoxymethylene (POM) exists.
- PMMA polymethyl methacrylate
- POM polyoxymethylene
- the crosslinkable layer B becomes photochemical before the engraving recording (actinic radiation), thermally or by means of electron beams networked.
- the crosslinkable layer B) can also have a multilayer structure be, wherein at least one engravable material layer is provided which, in addition to the at least one polymeric binder B3) a polymeric filler B4) with a ceiling temperature of contains less than 800 K, in particular less than 600 K.
- additives e.g. Dyes, stabilizers or Plasticizer be incorporated.
- the coherent electromagnetic radiation for engraving recording is expediently laser radiation, in particular the radiation from a CO 2 laser.
- laser radiation in particular the radiation from a CO 2 laser.
- the filler B4) is in the form of pre-crosslinked or uncrosslinked polymer beads with diameters in Range of about 5-10 microns to the binder B3) is added.
- the Size is preferably below the desired resolution of the fine relief elements of the relief.
- a printing plate with a material according to the invention and a laser engraving, produced by means of a CO 2 laser with a wavelength of 10640 nm and a power of over 100 W with a focus diameter of approx. 15 ⁇ m, is characterized in that with a halftone engraving the Pressure plate the intermediate depths between about 15 and about 50 microns, in particular in the range of about 24 to about 45 microns.
- the print products manufactured with it thus meet the highest demands of printing technology.
- a printing plate with a material according to the invention is characterized by a filler which is contained as particles and / or beads in the crosslinked layer B).
- Binders for the engraving material are polyvinyl alcohol a degree of hydrolysis of 50-99% and / or copolymers of Polyvinyl alcohol with the structural unit mentioned in claim 1. The production and use of such polyvinyl alcohols and / or copolymers are described in the examples. There are polymeric binders which can also be used advantageously contain at least one reactive group attached to a chemical Participate in response to networking the recording layer can.
- Reactive groups in the side chain are also suitable of a branched homopolymer or copolymer, or subsequently introduced into the polymer via a polymer-analogous modification reactive groups such as described in EP-A 0079514, EP-A 0224164, or EP-A 0059988, the first two documents Binder, a polyvinyl alcohol derivative or a polylakylene oxide-vinyl ester graft copolymer with ethanol and Vinylester structural units describe and the last script as a photoinitiator an acylphosphine oxide compound for photopolymerizable Describes recording masses.
- Materials from the polymers mentioned or theirs are preferred Mixtures that are cross-linked.
- Networking can be achieved through a chemical reaction, e.g. a radical, ionic or coordinative polymerization, a polycondensation or Polyaddition.
- the crosslinking reaction can initiated photochemically or thermally, if necessary also with Using a low molecular weight compound with reactive groups and / or a suitable initiator, or by means of an electron beam be performed.
- the manufacture of the material for engraving recording before Laser engraving can be carried out according to one of the known manufacturing processes, such as e.g. Pouring a solution of the polymers and possibly other Starting materials from a suitable solvent or Solvent mixture or by extrusion.
- the material was placed on rollers with a nominal size applied by 40 cm and the same depending on the material Circumferential speeds of approx. 55/110/165/220 rpm rotated to Laser engraving.
- the focus of the Laser beam adjusted on the material surface.
- a partially hydrolyzed polyvinyl alcohol KP 405 from Kuraray co. Ltd., Japan
- This material is laminated onto a coated PET film and the layer thus obtained with a total thickness of 1050 ⁇ m is dried for three hours at 60 ° C. in a drying cabinet.
- the light-sensitive layer is then irradiated with UV light for 20 minutes and thus crosslinked.
- the cross-linked material is then engraved with a CO 2 laser under the conditions mentioned. engraving speed 55.84 rpm Result s. Table 1 rating Excellent printing results, but the long engraving time of 120 min is disadvantageous.
- Material according to Example 1 crosslinked, additionally contains 5% by weight crosslinked PMMA beads with an average particle diameter of approx. 5 ⁇ m, for example AgfaPearl® x 5000 from Agfa-Gevaert AG, with a special dispersion coating.
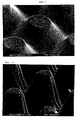
- AgfaPearl® is a registered trademark of Agfa-Gevaert AG, Leverkusen. engraving speed 111.68 rpm Result s. Table 1 and SEM image, Fig. 1 Intermediate depth at 50% tone value about 39 ⁇ m (at 223.36 rpm about 18 ⁇ m) rating Excellent printing results, slightly longer engraving time of 60 minutes compared to conventional production.
- Crosslinked material according to Example 1 additionally contains 10% by weight of crosslinked PMMA beads with an average particle diameter of approximately 5 ⁇ m. engraving speed 223.36 rpm Result s. Table 1 and SEM image, Fig. 2 Intermediate depth at a tone value of 50% about 24 ⁇ m (at 111.68 rpm about 45 ⁇ m) rating Excellent printing results, production time of 30 minutes is even significantly shorter than conventional!
- the figures Fig. 1 and 2 show greatly enlarged relief views of laser engraving plates according to the invention, which were engraved with different roller speeds.
- the Ultraform N 2520 X L2 from Ultraform GmbH, Ludwigshafen, with conductive carbon black in granular form was used as the POM material.
- the granules were very finely ground in a ball mill and the ground material was then sieved to an average particle size of approximately 5 ⁇ m before being introduced into the crosslinkable layer B) of the material.
- the finished material was engraved with a Nd: YAG laser with a wavelength of 1064 nm from Baasel-Scheel.
- the focus diameter of the IR beam was set to 20 ⁇ m.
- Example 1 Material according to Example 1 with the difference that the batch solution was not laminated to a film and dried. Rather, the solution was used to coat a cylinder, for example consisting of a GRP core and a PU structure, and to dry the cylinder thus provided with a light-sensitive layer for three hours at 60 ° C. in a drying cabinet. The light-sensitive layer is then irradiated with UV light for 20 minutes and thus crosslinked. The cross-linked material is then engraved with a CO 2 laser under the conditions mentioned. Result s. Table 1 rating Excellent printing results, very short production time of 40 minutes.
- Material made from 55 parts by weight of a copolymer of vinyl alcohol and ethylene glycol (described for example in DE 28 46 647 A1), 8 parts by weight of a plasticizer suitable for polyvinyl alcohol, for example polyethylene glycol (for example Pluriol E 400 from BASF AG), 24 parts by weight of a phenylglycidyl ether acrylate as an ethylenically unsaturated compound , 10 parts by weight of crosslinked PMMA beads with an average particle diameter of approx.
- a bis (N-methylolacrylamido) ethylene glycol ether are added as ethylenically unsaturated compound, 2 parts by weight of benzil dimethyl ketal as initiator, 0.2 part by weight of the potassium salt of N-
- This solution is adjusted to a concentration of 45% solids and then poured onto a film support in such a way that a 600 ⁇ m thick photosensitive layer results after drying.
- This material is laminated onto a coated PET film and the layer thus obtained, with a total thickness of 1050 ⁇ m, is dried for three hours at 60 ° C. in a drying cabinet.
- the light-sensitive layer is then irradiated with UV light for 20 minutes and thus crosslinked.
- the cross-linked material is then engraved with a CO 2 laser under the conditions mentioned. Result s.
- Table 1 rating Material melts during the engraving process, melted, crater-like material remains, unusable printing result
- a copolymer of vinyl alcohol and ethylene glycol for example described in DE 28 46 647 A1
- This solution is adjusted to a concentration of 40% solids with a water / n-propanol mixture (60/40 parts by weight) and then poured onto a film support in such a way that a 600 ⁇ m thick photosensitive layer results after drying ,
- This material is laminated onto a coated PET film and the layer thus obtained, with a total thickness of 1050 ⁇ m, is dried for three hours at 60 ° C. in a drying cabinet.
- the light-sensitive layer is exposed through a test negative in a UV vacuum exposure unit (Nyloprint exposure unit 80 x 107) and washed out with water (Nyloprint washout system DW 85). Result s. Table 1 and SEM image, Fig. 3 rating good printing result
- Figure 4 shows compared to a conventional, according to the Nylopring® process, pressure plate produced in Fig. 3 a laser engraved printing plate according to the invention with the same Characteristic values 48 L / cm screen ruling and tonal values of 20%.
- NYLOPRINT ® is a registered trademark of BASF Drucksysteme GmbH, Stuttgart.
- binder filler [Wt .-%] laser source engraving result needed time [Min] print results 1 PVA 0 CO 2 ++ 120 ++ 2 PVA 5 CO 2 ++ 60 ++ 3 PVA 10 CO 2 ++ 30 ++ 3A PVA 10 Nd: YAG + 40 + 4 PVA 10 CO 2 ++ 30 ++ 5 PVA 10 CO 2 ++ 35 ++ V1 PA 0 CO 2 - - 60 - - V2 PVA 0 conv. kG 45 +
Landscapes
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Plasma & Fusion (AREA)
- Manufacturing & Machinery (AREA)
- Printing Plates And Materials Therefor (AREA)
- Manufacture Or Reproduction Of Printing Formes (AREA)
- Printing Methods (AREA)
Description

| Gravurgeschwindigkeit | 55,84 U/min |
| Ergebnis | s. Tabelle 1 |
| Bewertung | Hervorragende Druckergebnisse, nachteilig allerdings die lange Gravurzeit von 120 min. |
| Gravurgeschwindigkeit | 111,68 U/min |
| Ergebnis | s. Tabelle 1 und REM-Aufnahme, Abb. 1 Zwischentiefe bei Tonwert 50 % etwa 39 µm (bei 223,36 U/min etwa 18 µm) |
| Bewertung | Hervorragende Druckergebnisse,etwas höhere Gravurzeit von 60 min gegenüber konventioneller Herstellung. |
| Gravurgeschwindigkeit | 223,36 U/min |
| Ergebnis | s. Tabelle 1 und REM-Aufnahme, Abb. 2 Zwischentiefe bei Tonwert 50 % etwa 24 µm (bei 111,68 U/min etwa 45 µm) |
| Bewertung | Hervorragende Druckergebnisse, Herstellungszeit mit 30 min sogar wesentlich kürzer als konventionell! |
| Ergebnis | s. Tabelle |
| Bewertung | Gute Druckergebnisse mit sehr geringer Tonwertzunahme in kurzer Herstellzeit. |
| Ergebnis | s. Tabelle 1 |
| Bewertung | Hervorragende Druckergebnisse, sehr kurze Herstellungszeit von 40 min. |
| Ergebnis | s. Tabelle 1 |
| Bewertung | Hervorragende Druckergebnisse, sehr kurze Herstellungszeit von 35 min. |
| Ergebnis | s. Tabelle 1 |
| Bewertung | Material schmilzt während des Gravurvorgangs, geschmolzenes, kraterförmig aufgeworfenes Material bleibt zurück, unbrauchbares Druckergebnis |
| Ergebnis | s. Tabelle 1 und REM-Aufnahme, Abb. 3 |
| Bewertung | gutes Druckergebnis |
| Bsp. | Bindemittel | Füllstoff [Gew.-%] | Laserquelle | Gravurergebnis | benötigte zeit [min] | Druckergebnis |
| 1 | PVA | 0 | CO2 | ++ | 120 | ++ |
| 2 | PVA | 5 | CO2 | ++ | 60 | ++ |
| 3 | PVA | 10 | CO2 | ++ | 30 | ++ |
| 3A | PVA | 10 | Nd:YAG | + | 40 | + |
| 4 | PVA | 10 | CO2 | ++ | 30 | ++ |
| 5 | PVA | 10 | CO2 | ++ | 35 | ++ |
| V1 | PA | 0 | CO2 | - - | 60 | - - |
| V2 | PVA | 0 | konv. | k.G. | 45 | + |
Claims (12)
- Verfahren zur Herstellung einer Hochdruckplatte umfassend die folgenden Schritte:(a) Photochemische, thermische oder Elektronenstrahl-Vernetzung eines Materials für die Gravur-Aufzeichnung mittels kohärenter elektromagnetischer Strahlung, bestehend auswobei die vernetzbare Schicht B)A) einem Träger,B) einer vernetzbaren Schicht,C) optional einer Deckschicht,D) optional einer Deckfolie,B1) mindestens eine ethylenisch ungesättigte Verbindung undB2) einen Polymerisations-Initiator, sowieB3) wenigstens ein polymeres Bindemittel enthält, das aus einem Polyvinylalkohol mit einem Hydrolysegrad von 50 - 99 % und/oder einem oder mehreren Copolymeren besteht, die in einem spezifischen Anteil die Struktureinheitaufweisen, dadurch gekennzeichnet, daß
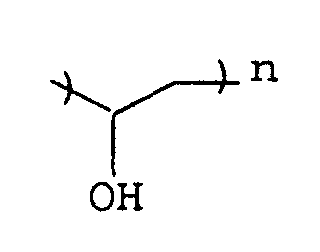 B4) außerdem ein polymerer Füllstoff vorgesehen ist, der eine Ceiling-Temperatur kleiner als 800 K, insbesondere kleiner als 600 K aufweist, sowie(b) Gravur Aufzeichnung des Materials mittels kohärenter elektromagnetischer Strahlung.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, daß der polymere Füllstoff vernetzt oder unvernetzt ist.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß der polymere Füllstoff aus einem oder mehreren der folgenden Polymeren besteht: Polystyrol, Polymethylmethacrylat, Poly(ethylen)keton, Polyoxymethylen und Poly(α-methylstyrol).
- Verfahren nach einem der Ansprüche 1 bis 3, gekennzeichnet durch einen Füllstoff in Partikelform, insbesondere in Kugelform oder Etwa-Kugelform, wobei die größte Abmessung ca. 5-10 µm beträgt.
- Verfahren nach einem oder mehreren der Ansprüche 1 bis 4, dadurch gekennzeichnet, daß der polymere Füllstoff mit einem Gewichtsprozentanteil von 1 bis 49,9 %, insbesondere von 2 bis 25 %, vorzugsweise von 5-15 %, bezogen auf den Feststoffanteil der vernetzbaren Schicht B) verwendet wird.
- Verfahren nach einem oder mehreren der Ansprüche 1 bis 5, dadurch gekennzeichnet, daß der polymere Füllstoff eine Ceiling-Temperatur von kleiner 500 K aufweist und insbesondere aus Polymethylmethacrylat oder aus Polyoxymethylen besteht.
- Verfahren nach einem der Ansprüche 1 bis 6, dadurch gekennzeichnet, daß die vernetzbare Schicht (B) mehrschichtig ausgebildet ist und mindestens eine gravierbare Material-Schicht vorgesehen ist, die, außer dem wenigstens einen polymeren Bindemittel.B3), polymerer Füllstoff mit einer Ceiling-Temperatur von kleiner als 800 K, insbesondere kleiner als 600 K enthält.
- Verfahren nach einem oder mehreren der Ansprüche 1 bis 7, dadurch gekennzeichnet, daß ein oder mehrere Zusatzstoffe, wie z.B. Farbstoffe, Stabilisatoren oder Weichmacher eingearbeitet sind.
- Verfahren nach einem oder mehreren der Ansprüche 1 bis 8, gekennzeichnet durch vorvernetzte Polymerkügelchen aus PMMA als Füllstoff mit einem mittleren Durchmesser von ca. 5 µm.
- Verfahren nach einem oder mehreren der Ansprüche 1 bis 8, gekennzeichnet durch unvernetzte Polymer-Partikel aus POM als Füllstoff, mit einer mittleren größten Abmessung von ca. 5 µm.
- Verfahren nach einem oder mehreren der Ansprüche 1 bis 10, dadurch gekennzeichnet, daß die kohärente elektromagnetische Strahlung Laserstrahlung, insbesondere die Strahlung eines CO2-Lasers ist.
- Druckplatte hergestellt mittels eines Verfahrens gemäß Anspruch 10, wobei der CO2-Laser mit der Wellenlänge von 10 640 nm eine Leistung von.über 100 W bei einem Fokus-Durchmesser von ca. 15 µm aufweist, dadurch gekennzeichnet, daß bei einer Halbton-Gravur der Druckplatte die Zwischentiefen zwischen ca. 15 und ca. 50 µm, insbesondere im Bereich von etwa 24 bis ca 45 µm liegen.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19838315 | 1998-08-24 | ||
| DE19838315A DE19838315A1 (de) | 1998-08-24 | 1998-08-24 | Material für die Gravur-Aufzeichnung mittels kohärenter elektromagnetischer Strahlung und Druckplatte damit |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0982124A2 EP0982124A2 (de) | 2000-03-01 |
| EP0982124A3 EP0982124A3 (de) | 2001-09-26 |
| EP0982124B1 true EP0982124B1 (de) | 2004-04-21 |
Family
ID=7878475
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99116468A Expired - Lifetime EP0982124B1 (de) | 1998-08-24 | 1999-08-21 | Verfahren zur Herstellung von Hochdruckplatten durch Gravur-Aufzeichnung mittels kohärenter elektromagnetischer Strahlung und damit hergestellte Druckplatte |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US6214521B1 (de) |
| EP (1) | EP0982124B1 (de) |
| JP (1) | JP2000168253A (de) |
| DE (2) | DE19838315A1 (de) |
Families Citing this family (28)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1136254B1 (de) * | 2000-03-23 | 2003-05-28 | BASF Drucksysteme GmbH | Verwendung von Pfropfcopolymeren zur Herstellung lasergravierbarer Reliefdruckelementen |
| DE10040928A1 (de) | 2000-08-18 | 2002-02-28 | Basf Drucksysteme Gmbh | Verfahren zur Herstellung lasergravierbarer Flexodruckelemente auf flexiblen metallischen Trägern |
| AUPR857301A0 (en) * | 2001-10-29 | 2001-11-29 | Kirk Engineering Services Australia Pty Ltd | Printing elements and methods of construction |
| JP2003191697A (ja) * | 2001-12-12 | 2003-07-09 | Ichika Kokusai Kagi Kofun Yugenkoshi | 透かし彫り用紙及びその彫刻方法 |
| US6806018B2 (en) | 2002-03-25 | 2004-10-19 | Macdermid Graphic Arts, Inc. | Processless digitally imaged printing plate using microspheres |
| US6989220B2 (en) | 2002-03-25 | 2006-01-24 | Macdermid Printing Solutions, Llc | Processless digitally imaged photopolymer elements using microspheres |
| JP2004136674A (ja) * | 2002-10-17 | 2004-05-13 | Hell Gravure Systems Gmbh | 凹版印刷に用いられる印刷版を製造するための方法、凹版印刷に用いられる印刷版およびその使用 |
| US7550249B2 (en) | 2006-03-10 | 2009-06-23 | Az Electronic Materials Usa Corp. | Base soluble polymers for photoresist compositions |
| US7759046B2 (en) | 2006-12-20 | 2010-07-20 | Az Electronic Materials Usa Corp. | Antireflective coating compositions |
| DE102007015263A1 (de) * | 2007-03-27 | 2008-10-02 | Hell Gravure Systems Gmbh & Co. Kg | Hochdruckform, insbesondere Flexodruckform, und Verfahren zu ihrer Herstellung |
| US7732118B2 (en) * | 2007-05-10 | 2010-06-08 | Eastman Kodak Company | Negative-working imageable elements and methods of use |
| JP2009023181A (ja) * | 2007-07-18 | 2009-02-05 | Tokyo Ohka Kogyo Co Ltd | 樹脂組成物、印刷原版、および印刷原版の製造方法 |
| JP5401026B2 (ja) | 2007-09-26 | 2014-01-29 | 富士フイルム株式会社 | レーザー彫刻用樹脂組成物、レーザー彫刻用樹脂印刷版原版、レリーフ印刷版およびレリーフ印刷版の製造方法 |
| EP2058123B1 (de) | 2007-11-08 | 2012-09-26 | FUJIFILM Corporation | Harzdruckplattenvorläufer für die Lasergravur, Reliefdruckplatte und Verfahren zur Herstellung der Reliefdruckplatte |
| JP5500831B2 (ja) | 2008-01-25 | 2014-05-21 | 富士フイルム株式会社 | レリーフ印刷版の作製方法及びレーザー彫刻用印刷版原版 |
| JP5241252B2 (ja) | 2008-01-29 | 2013-07-17 | 富士フイルム株式会社 | レーザー彫刻用樹脂組成物、レーザー彫刻用レリーフ印刷版原版、レリーフ印刷版及びレリーフ印刷版の製造方法 |
| JP5137618B2 (ja) | 2008-02-28 | 2013-02-06 | 富士フイルム株式会社 | レーザー彫刻用樹脂組成物、レーザー彫刻用レリーフ印刷版原版、レリーフ印刷版及びレリーフ印刷版の製造方法 |
| JP5409045B2 (ja) | 2008-02-29 | 2014-02-05 | 富士フイルム株式会社 | レーザー彫刻用樹脂組成物、レーザー彫刻用樹脂印刷版原版、レリーフ印刷版およびレリーフ印刷版の製造方法 |
| JP5322575B2 (ja) | 2008-03-28 | 2013-10-23 | 富士フイルム株式会社 | レーザー彫刻用樹脂組成物、画像形成材料、レーザー彫刻用レリーフ印刷版原版、レリーフ印刷版、及びレリーフ印刷版の製造方法 |
| US20090311494A1 (en) | 2008-06-17 | 2009-12-17 | Fujifilm Corporation | Relief printing plate precursor for laser engraving, relief printing plate, and process for producing relief printing plate |
| JP5404111B2 (ja) | 2008-07-18 | 2014-01-29 | 富士フイルム株式会社 | レーザー彫刻用樹脂組成物、画像形成材料、レーザー彫刻用レリーフ印刷版原版、レリーフ印刷版、及びレリーフ印刷版の製造方法 |
| US20100075117A1 (en) | 2008-09-24 | 2010-03-25 | Fujifilm Corporation | Relief printing plate precursor for laser engraving, method of producing the same, relief printing plate obtainable therefrom, and method of producing relief printing plate |
| US8941028B2 (en) * | 2012-04-17 | 2015-01-27 | Eastman Kodak Company | System for direct engraving of flexographic printing members |
| WO2014129243A1 (ja) | 2013-02-20 | 2014-08-28 | 東レ株式会社 | レーザー彫刻用樹脂印刷原版 |
| TWI589459B (zh) * | 2014-09-26 | 2017-07-01 | Daigin Chemical Co Ltd | Water pressure transfer method for producing relief touch |
| JP6318132B2 (ja) * | 2015-11-11 | 2018-04-25 | 株式会社有沢製作所 | 着色感光性樹脂組成物 |
| JP6466549B2 (ja) * | 2017-11-28 | 2019-02-06 | 株式会社有沢製作所 | 着色感光性樹脂組成物 |
| CN114683675B (zh) * | 2020-12-28 | 2023-11-14 | 乐凯华光印刷科技有限公司 | 一种表面自带纹理的平顶网点的柔性树脂版及其制版方法 |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2909992A1 (de) | 1979-03-14 | 1980-10-02 | Basf Ag | Photopolymerisierbare aufzeichnungsmassen, insbesondere zur herstellung von druckplatten und reliefformen |
| DE2846647A1 (de) | 1978-10-26 | 1980-05-08 | Basf Ag | Photopolymerisierbare mischung fuer die herstellung von druck- und reliefformen |
| DE3144905A1 (de) * | 1981-11-12 | 1983-05-19 | Basf Ag, 6700 Ludwigshafen | Zur herstellung von druck- und reliefformen geeignetes lichtempfindliches auszeichnungsmaterial und verfahren zur herstellung von druck- und reliefformen mittels dieses aufzeichnungsmaterials |
| US4551415A (en) * | 1982-04-22 | 1985-11-05 | E. I. Du Pont De Nemours And Company | Photosensitive coatings containing crosslinked beads |
| DE3541162A1 (de) | 1985-11-21 | 1987-05-27 | Basf Ag | Photoempfindliche aufzeichnungsmaterialien mit elastomeren pfropfcopolymerisat-bindemitteln sowie reliefformen daraus |
| JP2793068B2 (ja) * | 1991-04-24 | 1998-09-03 | 日本ペイント株式会社 | 感光性樹脂組成物 |
| US5262476A (en) * | 1992-03-10 | 1993-11-16 | The Dow Chemical Company | Polycarbonate/polyester blends modified with poly(phenylene ether) |
| US5798202A (en) * | 1992-05-11 | 1998-08-25 | E. I. Dupont De Nemours And Company | Laser engravable single-layer flexographic printing element |
| JPH06230568A (ja) * | 1993-02-01 | 1994-08-19 | Nippon Synthetic Chem Ind Co Ltd:The | 感光性樹脂組成物 |
| US5563023A (en) * | 1994-11-02 | 1996-10-08 | Minnesota Mining And Manufacturing Co. | Photoimageable elements |
| DE19536808A1 (de) | 1995-10-02 | 1997-04-03 | Basf Lacke & Farben | Verfahren zur Herstellung von photopolymeren Hochdruckplatten |
| EP0773112B1 (de) * | 1995-11-09 | 2001-05-30 | Agfa-Gevaert N.V. | Wärmeempfindliches Aufzeichnungselement und Verfahren zur Herstellung einer Druckform damit |
-
1998
- 1998-08-24 DE DE19838315A patent/DE19838315A1/de not_active Withdrawn
-
1999
- 1999-08-21 DE DE59909221T patent/DE59909221D1/de not_active Expired - Fee Related
- 1999-08-21 EP EP99116468A patent/EP0982124B1/de not_active Expired - Lifetime
- 1999-08-23 JP JP11274945A patent/JP2000168253A/ja active Pending
- 1999-08-24 US US09/382,149 patent/US6214521B1/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| EP0982124A3 (de) | 2001-09-26 |
| JP2000168253A (ja) | 2000-06-20 |
| EP0982124A2 (de) | 2000-03-01 |
| DE59909221D1 (de) | 2004-05-27 |
| US6214521B1 (en) | 2001-04-10 |
| DE19838315A1 (de) | 2000-03-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0982124A2 (de) | Material für die Gravur-Aufzeichnung mittels kohärenter elektromagnetischer Strahlung und Druckplatte damit | |
| EP1136254B1 (de) | Verwendung von Pfropfcopolymeren zur Herstellung lasergravierbarer Reliefdruckelementen | |
| EP0767407B2 (de) | Verfahren zur Herstellung von Flexodruckplatten unter Verwendung eines durch digitale Informationsübertragung geeigneten mehrschichtigen Aufzeichnungselements | |
| DE69308570T2 (de) | Flexodruckelement mit einer durch ir-bestrahlung ablativen schicht und verfahren zur herstellung einer flexodruckplatten | |
| EP1014194B1 (de) | Photopolymerisierbare Druckformen mit Oberschicht zur Herstellung von Reliefdruckformen | |
| DE69605236T2 (de) | Flexodruckelement mit einer durch IR-Bestrahlung ablativen Schicht und Verfahren zur Herstellung einer Flexodruckplatte | |
| EP1423280B1 (de) | Verfahren zur herstellung von flexodruckformen mittels laser-direktgravur | |
| DE69817345T2 (de) | Digitale druckplatte mit einer thermischen maske | |
| EP3304203B1 (de) | Digital bebilderbare flexodruckplatte mit integraler barriereschicht | |
| DE2542815C2 (de) | Verfahren zur Herstellung von Druckformen auf fotomechanischem Wege | |
| DE1140080B (de) | Platte zur Erzeugung von Reliefdruckformen durch Photopolymerisation | |
| EP1381511B1 (de) | Lasergravierbare flexodruckelemente mit reliefbildenden elastomeren schichten enthaltend syndiotaktisches 1,2-polybutadien | |
| WO2002016134A1 (de) | Verfahren zur herstellung lasergravierbarer flexodruckelemente auf flexiblen metallischen trägern | |
| DE19913560A1 (de) | Flexographische Druckplatte mit Maskenschicht und Bildgebungs- und Druckverfahren | |
| DE10061116A1 (de) | Fotoempfindliches flexographisches Druckelement mit mindestens zwei IR-ablativen Schichten | |
| EP0432713B1 (de) | Verfahren zur Herstellung von Bildern auf tonbaren lichtempfindlichen Schichten | |
| DE10061114A1 (de) | Fotoempfindliches flexographisches Druckelement mit Polyether-Polyurethane umfassender IR-ablativer Schicht | |
| DE69820219T2 (de) | Formbeständige Lithographie-Druckplatten mit Sol-Gel-Schicht | |
| DE60109913T2 (de) | Lithographische druckplatte | |
| DE1276727B (de) | Verfahren zur Speicherung und Rueckgewinnung von Informationen | |
| EP0992849B1 (de) | Photopolymerisierbare Druckformen zur Herstellung von Reliefdruckplatten für den Druck mit UV-härtbaren Druckfarben | |
| EP0565818A2 (de) | Verfahren zur photochemischen oder mechanischen Herstellung flexibler Druckformen | |
| DE3128949A1 (de) | Lichtempfindliche aufzeichnungsmaterialien zur herstellung von abriebs- und kratzfesten tiefdruckformen sowie verfahren zur herstellung von tiefdruckformen mittels dieser aufzeichnungsmaterialien | |
| DE69202230T2 (de) | Sperrschicht für mehrschichtiges wärmeempfindliches bildförmendes Medium. | |
| DE2302463B2 (de) | Flexibler Zurichtebogen und Verfahren zur Herstellung einer Zurichtung daraus |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE Kind code of ref document: A2 Designated state(s): DE FR GB IT |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Free format text: 7B 41C 1/10 A, 7B 41C 1/05 B, 7B 41N 1/12 B |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20010912 |
|
| AKX | Designation fees paid |
Free format text: DE FR GB IT |
|
| 17Q | First examination report despatched |
Effective date: 20021010 |
|
| RTI1 | Title (correction) |
Free format text: PROCESS FOR MAKING LETTERPRESS PLATE BY ENGRAVING USING COHERENT ELECTROMAGNETIC RADIATION, AND PRINTING PLATE PREPARED T |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RTI1 | Title (correction) |
Free format text: PROCESS FOR MAKING LETTERPRESS PLATE BY ENGRAVING USING COHERENT ELECTROMAGNETIC RADIATION, AND PRINTING PLATE PREPARED T |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB IT |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REF | Corresponds to: |
Ref document number: 59909221 Country of ref document: DE Date of ref document: 20040527 Kind code of ref document: P |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20040526 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20040810 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20040818 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20040902 Year of fee payment: 6 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20050124 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050821 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060301 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20050821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050831 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20111125 |