EP0935004B1 - Perfectionnements apportés aux fours de refroidissement pour produits en bande - Google Patents
Perfectionnements apportés aux fours de refroidissement pour produits en bande Download PDFInfo
- Publication number
- EP0935004B1 EP0935004B1 EP99400142A EP99400142A EP0935004B1 EP 0935004 B1 EP0935004 B1 EP 0935004B1 EP 99400142 A EP99400142 A EP 99400142A EP 99400142 A EP99400142 A EP 99400142A EP 0935004 B1 EP0935004 B1 EP 0935004B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- strip
- rollers
- heating elements
- furnace
- heating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000137 annealing Methods 0.000 title claims description 4
- 239000002184 metal Substances 0.000 title claims description 3
- 238000010438 heat treatment Methods 0.000 claims description 29
- 238000001816 cooling Methods 0.000 claims description 11
- 230000015572 biosynthetic process Effects 0.000 claims description 7
- 238000005246 galvanizing Methods 0.000 claims description 3
- 238000009434 installation Methods 0.000 claims description 3
- 230000000717 retained effect Effects 0.000 claims description 3
- 239000000919 ceramic Substances 0.000 claims description 2
- 238000012544 monitoring process Methods 0.000 claims 1
- 238000000034 method Methods 0.000 description 8
- 238000004519 manufacturing process Methods 0.000 description 4
- 230000003321 amplification Effects 0.000 description 3
- 238000009826 distribution Methods 0.000 description 3
- 230000000694 effects Effects 0.000 description 3
- 238000003199 nucleic acid amplification method Methods 0.000 description 3
- 238000004804 winding Methods 0.000 description 2
- 230000007423 decrease Effects 0.000 description 1
- 230000008030 elimination Effects 0.000 description 1
- 238000003379 elimination reaction Methods 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 238000007669 thermal treatment Methods 0.000 description 1
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/52—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for wires; for strips ; for rods of unlimited length
- C21D9/54—Furnaces for treating strips or wire
- C21D9/56—Continuous furnaces for strip or wire
- C21D9/573—Continuous furnaces for strip or wire with cooling
- C21D9/5735—Details
- C21D9/5737—Rolls; Drums; Roll arrangements
Definitions
- the present invention relates to improvements made to cooling implemented in thermal treatment installations strip metal products, in particular in annealing furnace systems or continuous galvanizing through which the strip to be treated is conveyed by through rollers
- the technical problem which the present invention proposes to solve is that the elimination of this risk of folds forming in the new strip, during the change of tape format, in such cooling chambers strip products.
- rollers such as 14 have a homogeneous temperature when changing band formats.
- it either cool the central part of the roll across the width of the strip, which is extremely difficult to achieve, either heating the parts of the roll outside the bandwidth.
- the invention proposes to provide a simple, effective and inexpensive solution to the problem mentioned above of the formation of folds when changing formats of bands.
- the invention relates to a device as defined in claim 1 making it possible to avoid the risk of formation of folds on a strip conveyed in a cooling oven of a continuous heat treatment installation, in particular an annealing or galvanizing, through which the strip is conveyed by rollers, these being heated by contact with the strip across its width, the risk of formation of folds occurring when changing band formats, when the next strip is wider, this then passing on rollers having retained the imprint of thermal expansion due to the previous strip, this device being characterized in that one positions: heating elements close rolls, and below them, over the entire width of the oven and, on the side of the rollers opposite said heating elements, aligned panels of so as to form with the wall of the oven, a warm chamber, the moving band continuous serving as a heat shield so that only the part of the roll not covered by the strip is heated by said heating elements.
- said elements heaters are made in the form of electric candles.
- the heating of the rollers, by said elements heating can be carried out continuously or discontinuously depending on the frequency of changing band formats, said heating elements operating continuously during frequent changes of formats and discontinuously during infrequent format changes, heating being used for a fixed period, immediately before the change of formats.
- the operation of said heating elements is controlled by a real-time calculator.
- FIG. 4 represents a cooling oven to which is applied the present invention.
- the device which is the subject of the invention therefore comprises heating elements such as 18 which are positioned near the rollers 14 as seen in Figure 4, in below these, over the entire width of the oven, these heating elements 18 can be made in the form of electric candles for example.
- the device further includes panels such as 20 which are aligned on the side of the rollers 14, opposite the heating elements 18, these panels being designed and arranged so as to form a warm chamber with the wall of the oven in order to increase heating efficiency.
- the panels 20 can be produced, inter alia, made of ceramic fibers taken between stainless sheets.
- the heating system such as 18 of the rollers 14 is controlled by a real-time computer.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Heat Treatment Of Strip Materials And Filament Materials (AREA)
- Coating With Molten Metal (AREA)
- Treatment Of Fiber Materials (AREA)
- Tunnel Furnaces (AREA)
Description
- ralentissement du défilement de la bande pendant le changement de formats : cette technique présente l'inconvénient d'impliquer une perte de production en raison de ce ralentissement ;
- chauffage des rouleaux à l'intérieur de ceux-ci, notamment par une résistance électrique interne : il en résulte en général une fabrication des rouleaux complexe et coûteuse et cette technique n'est utilisable que pour quelques formats de bandes ; par ailleurs, cette technique nécessite une très grande stabilité de la position de la bande sur les rouleaux.
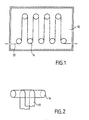
- La figure 1 est une vue schématique d'une enceinte de refroidissement à laquelle s'applique la présente invention ;
- La figure 2 est une vue partielle en perspective représentant l'enroulement de la bande à traiter sur un rouleau, cette figure ayant été utilisée dans le préambule de la présente description afin d'expliquer les motifs du risque de formation de plis de bande ;
- La figure 3a représente la répartition de la température le long de l'axe longitudinal des rouleaux ;
- La figure 3b représente la variation du diamètre du rouleau sous l'effet de la dilatation thermique (avec amplification) le long de l'axe longitudinal de ce rouleau, ces figures 3a et 3b ayant été commentées dans le préambule de la présente description et,
- La figure 4 est une vue partielle schématique représentant le dispositif objet de l'invention.
Claims (3)
- Dispositif permettant d'éviter le risque de formation de plis sur une bande véhiculée dans un four de refroidissement d'une installation de traitement thermique en continu, notamment un four de recuit ou de galvanisation, au travers duquel la bande est véhiculée par des rouleaux, ceux-ci étant chauffés par contact avec la bande dans la largeur de celle-ci, le risque de formation de plis se présentant lors d'un changement de formats de bandes, lorsque la bande suivante est plus large, celle-ci passant alors sur des rouleaux ayant conservé l'empreinte de la dilatation thermique due à la bande précédente, ce dispositif comportant des éléments chauffants (18) près des rouleaux (14), sur toute la largeur du four (10) et, sur le côté des rouleaux opposé auxdits éléments chauffants, des panneaux (20) alignés de manière à former avec la paroi du four, une chambre tiède, la bande (12) en déplacement continu servant d'écran thermique de manière que seule la partie du rouleau non recouverte par la bande soit chauffée par lesdits éléments chauffants, caractérisé en ce que les éléments chauffants (18) sont positionnés en dessous des rouleaux et en ce que le dispositif comporte des moyens de calculs en temps réel par un calculateur pour piloter le fonctionnement des dites éléments chauffants en fonction de formats de bandes et
ledit moyens de calculs en temps réel comportent de plus de moyens adaptés pour contrôler les éléments chauffants de façon continue lors de changements fréquents de formats, et de façon discontinue lors de changements peu fréquents de formats, le chauffage étant utilisé pendant une durée déterminée, immédiatement avant le changement de formats de bande. - Dispositif selon la revendication 1 caractérisé en ce que lesdits éléments chauffants (18) sont réalisés sous la forme de bougies électriques.
- Dispositif selon l'une quelconque des revendications précédentes caractérisé en ce que lesdits panneaux (20) sont réalisés en fibres céramiques prises entre des tôles inoxydables.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9801497 | 1998-02-09 | ||
| FR9801497A FR2774700B1 (fr) | 1998-02-09 | 1998-02-09 | Perfectionnements apportes aux fours de refroidissement pour produits en bande |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0935004A1 EP0935004A1 (fr) | 1999-08-11 |
| EP0935004B1 true EP0935004B1 (fr) | 2003-09-03 |
Family
ID=9522745
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99400142A Expired - Lifetime EP0935004B1 (fr) | 1998-02-09 | 1999-01-21 | Perfectionnements apportés aux fours de refroidissement pour produits en bande |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US6023048A (fr) |
| EP (1) | EP0935004B1 (fr) |
| JP (1) | JP3274843B2 (fr) |
| DE (2) | DE935004T1 (fr) |
| ES (1) | ES2138579T3 (fr) |
| FR (1) | FR2774700B1 (fr) |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5976830A (ja) * | 1982-10-23 | 1984-05-02 | Nippon Steel Corp | 連続熱処理炉の鋼帯ヒ−トバツクル防止方法 |
| JPS59207346A (ja) * | 1983-04-22 | 1984-11-24 | Fuji Photo Film Co Ltd | ウエブの巻取装置 |
| JPH062910B2 (ja) * | 1986-04-28 | 1994-01-12 | 三菱重工業株式会社 | 帯板支持ロ−ルの熱変形防止装置 |
| JPH02277727A (ja) * | 1989-04-19 | 1990-11-14 | Kawasaki Steel Corp | 冷却帯ロールの熱変形を防止した連続熱処理炉 |
| JPH0670259B2 (ja) * | 1989-06-16 | 1994-09-07 | 川崎製鉄株式会社 | 鋼帯の連続焼鈍方法 |
| US5230857A (en) * | 1989-11-22 | 1993-07-27 | Selas Corporation Of America | Strip elongation control in continuous annealing furnaces |
| JPH0819478B2 (ja) * | 1991-03-21 | 1996-02-28 | 新日本製鐵株式会社 | 帯板支持ロールの温度差変形防止構造 |
| FR2688802B1 (fr) * | 1992-03-19 | 1994-09-30 | Stein Heurtey | Procede de traitement thermique de bandes metalliques. |
| JPH083650A (ja) * | 1994-06-21 | 1996-01-09 | Nkk Corp | 金属帯の熱処理方法 |
| US5985212A (en) * | 1996-12-12 | 1999-11-16 | H-Technologies Group, Incorporated | High strength lead-free solder materials |
| JP5441009B2 (ja) | 2010-03-23 | 2014-03-12 | 富士ゼロックス株式会社 | 印刷制御装置、画像形成システムおよびプログラム |
-
1998
- 1998-02-09 FR FR9801497A patent/FR2774700B1/fr not_active Expired - Lifetime
-
1999
- 1999-01-21 DE DE0935004T patent/DE935004T1/de active Pending
- 1999-01-21 DE DE69910854T patent/DE69910854T2/de not_active Expired - Lifetime
- 1999-01-21 ES ES99400142T patent/ES2138579T3/es not_active Expired - Lifetime
- 1999-01-21 EP EP99400142A patent/EP0935004B1/fr not_active Expired - Lifetime
- 1999-01-21 US US09/234,442 patent/US6023048A/en not_active Expired - Fee Related
- 1999-02-03 JP JP02593399A patent/JP3274843B2/ja not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| EP0935004A1 (fr) | 1999-08-11 |
| ES2138579T3 (es) | 2004-03-16 |
| JP3274843B2 (ja) | 2002-04-15 |
| DE69910854T2 (de) | 2004-07-15 |
| FR2774700B1 (fr) | 2000-04-07 |
| DE935004T1 (de) | 2000-03-02 |
| DE69910854D1 (de) | 2003-10-09 |
| US6023048A (en) | 2000-02-08 |
| ES2138579T1 (es) | 2000-01-16 |
| JPH11315331A (ja) | 1999-11-16 |
| FR2774700A1 (fr) | 1999-08-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| FR2750949B1 (fr) | Protection contre la glace pour une structure poreuse | |
| JP2012514694A5 (fr) | ||
| TW200822982A (en) | Roll stand, rolling mill and method for rolling a metallic strip | |
| EP0345147A1 (fr) | Rouleau pour la manutention de produits sidérurgiques se déplaçant à l'intérieur d'un four | |
| EP0935004A1 (fr) | Perfectionnements apportés aux fours de refroidissement pour produits en bande | |
| FR3012870A1 (fr) | Procede de decongelation, rechauffage et/ou cuisson d'un produit alimentaire | |
| US9851144B2 (en) | Method and device for drying a fluid film applied to a substrate | |
| FR2575495A1 (fr) | Four de recuit continu de metaux | |
| FR2818488A3 (fr) | Element a temperature constante pour appareils chauffants, tels que grille-pain, fours et chauffe-eau | |
| FR2955462A1 (fr) | Dispositif de decongelation, rechauffage et cuisson d'un produit alimentaire, notamment d'une pate alimentaire surgelee | |
| EP1239053A1 (fr) | Rouleau destiné au transport d'une bande métallique dans une installation de recuit continu | |
| EP0037752B1 (fr) | Dispositif de guidage de matériau en bande et ses applications | |
| WO2015044587A1 (fr) | Procédé de cuisson de produits de boulangerie, viennoiserie et pâtisserie avec préchauffage direct, et ses dispositifs de mise en oeuvre | |
| BE1005166A5 (fr) | Arche de recuisson. | |
| JPS5520962A (en) | Rolling roll | |
| EP1647604B1 (fr) | Procedé et dispositif d'amélioration qualitative et quantitative de la production dans un four vertical de traitement de bandes d'acier ou d'aluminium | |
| KR101402547B1 (ko) | 유해물질 차단기능을 갖는 알루미늄 호일 | |
| FR2599483A1 (fr) | Four a zone de refroidissement lent | |
| EP1420209A3 (fr) | Radiateur de spectres sélectives | |
| FR2626592A1 (fr) | Procede de sechage et repassage de textiles plats faisant appel a l'energie electrique comme source de production de chaleur et installation pour sa mise en oeuvre | |
| CA2296196A1 (fr) | Appareil de cuisson et procede mettant en oeuvre un tel appareil | |
| WO2016142535A1 (fr) | Procédé de réduction du bruit du dégivrage d'une pompe à chaleur | |
| JP2004233768A (ja) | 定着装置 | |
| FR2483593A1 (fr) | Elements-diffuseurs pour dispositifs climatiseurs par surfaces | |
| JP2504269Y2 (ja) | イカのロ―スタ― |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): BE DE ES GB IT NL |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| RTI1 | Title (correction) |
Free format text: IMPROVED ANNEALING DEVICE FOR SHEET METAL |
|
| 17P | Request for examination filed |
Effective date: 19990904 |
|
| ITCL | It: translation for ep claims filed |
Representative=s name: BARZANO' E ZANARDO MILANO S.P.A. |
|
| GBC | Gb: translation of claims filed (gb section 78(7)/1977) | ||
| TCNL | Nl: translation of patent claims filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: BA2A Ref document number: 2138579 Country of ref document: ES Kind code of ref document: T1 |
|
| DET | De: translation of patent claims | ||
| AKX | Designation fees paid |
Free format text: BE DE ES GB IT NL |
|
| 17Q | First examination report despatched |
Effective date: 20021008 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): BE DE ES GB IT NL |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REF | Corresponds to: |
Ref document number: 69910854 Country of ref document: DE Date of ref document: 20031009 Kind code of ref document: P |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20031118 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2138579 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040604 |
|
| NLT1 | Nl: modifications of names registered in virtue of documents presented to the patent office pursuant to art. 16 a, paragraph 1 |
Owner name: SOLLAC Owner name: FIVES STEIN SOCIETE ANONYME |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20101224 Year of fee payment: 13 Ref country code: GB Payment date: 20101230 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20110103 Year of fee payment: 13 Ref country code: IT Payment date: 20101228 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20101221 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20110111 Year of fee payment: 13 |
|
| BERE | Be: lapsed |
Owner name: FIVE STEIN Effective date: 20120131 Owner name: SOLLAC Effective date: 20120131 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20120801 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20120121 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120801 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120121 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69910854 Country of ref document: DE Effective date: 20120801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120121 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120801 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20130708 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120122 |