WO2025004844A1 - 保護コーティング組成物 - Google Patents
保護コーティング組成物 Download PDFInfo
- Publication number
- WO2025004844A1 WO2025004844A1 PCT/JP2024/021615 JP2024021615W WO2025004844A1 WO 2025004844 A1 WO2025004844 A1 WO 2025004844A1 JP 2024021615 W JP2024021615 W JP 2024021615W WO 2025004844 A1 WO2025004844 A1 WO 2025004844A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- coating composition
- protective coating
- meth
- acrylate
- urethane
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08F—MACROMOLECULAR COMPOUNDS OBTAINED BY REACTIONS ONLY INVOLVING CARBON-TO-CARBON UNSATURATED BONDS
- C08F290/00—Macromolecular compounds obtained by polymerising monomers on to polymers modified by introduction of aliphatic unsaturated end or side groups
- C08F290/02—Macromolecular compounds obtained by polymerising monomers on to polymers modified by introduction of aliphatic unsaturated end or side groups on to polymers modified by introduction of unsaturated end groups
- C08F290/06—Polymers provided for in subclass C08G
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D175/00—Coating compositions based on polyureas or polyurethanes; Coating compositions based on derivatives of such polymers
- C09D175/04—Polyurethanes
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D4/00—Coating compositions, e.g. paints, varnishes or lacquers, based on organic non-macromolecular compounds having at least one polymerisable carbon-to-carbon unsaturated bond ; Coating compositions, based on monomers of macromolecular compounds of groups C09D183/00 - C09D183/16
Definitions
- the present disclosure relates to a protective coating composition.
- LEPs leading edge protection materials
- Patent document 1 (US 2020/0040869) describes a method of applying a protective layer to an outer surface of a wind turbine rotor blade. The method includes preparing a protective layer for application to the outer surface of the rotor blade, providing an air outlet channel between the rotor blade and the protective layer, attaching the protective layer to the outer surface of the rotor blade, and extracting air through the air outlet channel.
- Patent Document 2 (WO 2012/102294) describes a wing body that is made of fiber-reinforced plastic (FRP) and has a laminated protective sheet adhered to at least a portion of the leading edge of the wing body, the laminated protective sheet having, in order from the wing body side, an adhesive layer, an intermediate base fabric layer, and a durable surface layer.
- FRP fiber-reinforced plastic
- Patent document 3 (US 2021/0130647) describes a coating material composition used for the manufacture of erosion-stable coatings used as erosion protection, especially edge protection for rotor blades.
- the composition includes a stock component and a hardener component, where the stock component includes at least one trifunctional polycaprolactone polyol, at least one polycarbonate diol, or at least one trifunctional polycaprolactone polyol and polycarbonate diol, and the hardener component includes at least one crystallization-resistant isocyanate-functional prepolymer.
- Patent document 4 (WO 2016/075619) describes a method for making a protective cover for a wind turbine blade, characterized in that a) mixing a polyol and a butanediol, b) conditioning and degassing the mixture according to a), c) conditioning and degassing an isocyanate, d) pumping the degassed mixture according to b) and the degassed isocyanate according to c) through a mixhead into a mould, e) curing in the mould, and f) removing the cured article from the mould.
- Non-patent document 1 (Wind Energy Utilization Symposium, 2021, Vol. 43, p. 210) describes that when an erosion protection sheet is applied to a wind turbine blade, the step that occurs at the boundary between the wind turbine blade and the protection sheet reduces the aerodynamic characteristics of the wind turbine blade.
- Hirokazu Kawabata "Aerodynamic Performance Evaluation of Blades with Erosion Protection Sheets," Wind Energy Utilization Symposium, 2021, Vol. 43, p. 210
- the protective layer described in Patent Document 1 is a sheet that is applied in a later process after the blade is manufactured, and application is time-consuming. Furthermore, if the protective layer is applied in a later process, as described in Non-Patent Document 1, there is a risk that the aerodynamic characteristics of the blade will be reduced due to a step that occurs at the boundary between the protective layer and the blade.
- the laminated protective sheet described in Patent Document 2 is attached to the blade by an adhesive layer, and therefore the laminated protective sheet may peel off from the blade over long-term use, resulting in reduced aerodynamic characteristics or generating noise. If the thickness of the protective layer or laminated protective sheet is made, for example, 300 ⁇ m or more in order to ensure erosion resistance over a long period of time, the aerodynamic characteristics of the blade will be significantly reduced.
- Patent Document 3 The coating material composition described in Patent Document 3 has excellent workability, but because of its low curability, it is difficult to obtain a sufficient level of erosion resistance.
- Patent Document 4 requires that the protective cover be molded in advance to match the shape of the blade, which limits the blades that can be used.
- the thickness of the molded protective cover also tends to be large, which can easily lead to a decrease in the aerodynamic characteristics of the blade.
- the present disclosure provides a protective coating composition that requires little effort in application, prevents deterioration of aerodynamic characteristics, and is capable of forming an LEP with excellent erosion resistance.
- the inventors discovered that by using a resin composition containing a urethane resin having a urethane structure and a carbonate structure in the same molecule as a gel coat and leading edge protective agent during the manufacture of wind power blades, it is possible to reduce the amount of work required for application, avoid a decrease in aerodynamic characteristics, and impart an LEP with excellent erosion resistance to various types of wind power blades, thus completing the present invention.
- the present disclosure encompasses the following aspects:
- a protective coating composition comprising a urethane resin having a urethane structure and a carbonate structure in the same molecule, and an ethylenically unsaturated compound, the urethane resin is a urethane (meth)acrylate resin, A protective coating composition, wherein the cured product of said protective coating composition has an erosion resistance of 1.5 hours or more.
- Aspect 2 2.
- Aspect 3 3.
- the protective coating composition of claim 1 or 2 comprising 10% to 90% by weight of the urethane resin.
- the polycarbonate polyol has a number average molecular weight of 500 to 10,000.
- the polyisocyanate comprises a cycloaliphatic polyisocyanate.
- the wind power blade has a blade length of 10 m or more.
- LEPs with excellent erosion resistance can be formed on various types of wind power blades, with minimal construction effort and avoiding deterioration of aerodynamic characteristics.
- the protective coating composition of the present disclosure can also be used for various protective applications other than leading edge protection of wind power blades.
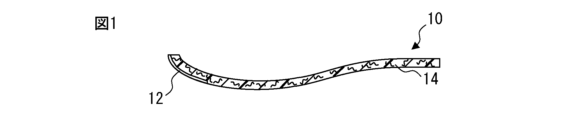
- FIG. 1 is a schematic cross-sectional view of a wind power generating blade according to an embodiment.
- FIG. 2 is an explanatory diagram of a method for manufacturing a wind power generation blade according to an embodiment using a vacuum-assisted impregnation method.
- (meth)acrylic means acrylic or methacrylic
- (meth)acrylate means acrylate or methacrylate
- (meth)acryloyloxy means acryloyloxy or methacryloyloxy.
- ethylenically unsaturated bond means a double bond formed between carbon atoms other than those forming an aromatic ring
- ethylenically unsaturated monomer means a monomer having an ethylenically unsaturated bond
- the "weight average molecular weight” and the “number average molecular weight” are values measured at room temperature (23°C) under the following conditions using gel permeation chromatography (GPC) and determined using a standard polystyrene calibration curve.
- Apparatus Shodex (trademark) GPC-101 (Resonac Co., Ltd.)
- a protective coating composition in one embodiment, includes a urethane resin having a urethane structure and a carbonate structure in the same molecule, and an ethylenically unsaturated compound.
- the urethane resin is a urethane (meth)acrylate resin
- the erosion resistance of the cured product of the protective coating composition is 1.5 hours or more.
- the erosion resistance is a value obtained by forming the cured product of the protective coating composition into a film having a thickness of 2 mm and evaluating the film according to the procedure described in the examples.
- the erosion resistance of the cured product of the protective coating composition is preferably 0.5 hours or more, more preferably 1.0 hours or more, and even more preferably 1.5 hours or more.
- the protective coating composition is a leading edge protectant for wind power blades.
- the formation and arrangement of a coating that can be used as a leading edge protective material can be performed during the manufacture of the wind power blade, thereby shortening the process and allowing the coating to be applied to wind power blades of various shapes.
- the coating can be heat cured in the heating step for hardening the matrix resin, a coating with high mechanical strength and bonding strength can be applied to the wind power blade.
- the coating is formed along the shape of the mold surface, it does not affect the aerodynamic characteristics of the wind power blade and can prevent a decrease in power generation efficiency.
- the use of the protective coating composition disclosed herein is not limited to the formation of a leading edge protective material for wind power blades.
- FIG. 1 is a schematic cross-sectional view of a wind power blade according to one embodiment.
- the wind power blade 10 is shown as a part and includes a fiber-containing substrate 14 and a coating 12 that is partially disposed on the leading edge side of the fiber-containing substrate 14.
- the surfaces of the coating 12 and the fiber-containing substrate 14 are continuous along the mold surface used in manufacturing the wind power blade 10, and there is no step at the boundary between the coating 12 and the fiber-containing substrate 14.
- the protective coating composition includes a urethane resin having a urethane structure and a carbonate structure in the same molecule.
- the urethane resin having a urethane structure and a carbonate structure in the same molecule has both high mechanical strength and excellent elongation properties. These properties of the urethane resin contribute to the excellent erosion resistance of the cured product of the protective coating composition.
- the urethane resin having a urethane structure and a carbonate structure in the same molecule can be obtained by polyaddition reaction of at least a polyisocyanate and a polyol, and at least one of the polyisocyanate and the polyol has a carbonate structure.
- the urethane resin may be used alone or in combination of two or more kinds.
- polyisocyanates include aromatic polyisocyanates such as 4,4'-diphenylmethane diisocyanate, 2,4-tolylene diisocyanate, 2,6-tolylene diisocyanate, 1,5-naphthalene diisocyanate, 3,3'-dimethyl-4,4'-biphenylene diisocyanate, polymethylene polyphenyl diisocyanate, xylylene diisocyanate, phenylene diisocyanate, and triphenylmethane triisocyanate; alicyclic polyisocyanates such as 4,4'-methylenebiscyclohexyl diisocyanate, isophorone diisocyanate, and cyclohexane-1,3-diylbis(methylene) diisocyanate; and aliphatic polyisocyanates such as hexamethylene diisocyanate and trimethylhexamethylene diisocyanate; as well as adducts, isocyan
- the polyisocyanate preferably contains an alicyclic polyisocyanate, and more preferably contains at least one selected from the group consisting of 4,4'-methylenebiscyclohexyl diisocyanate and isophorone diisocyanate.
- polycarbonate polyol which can introduce a carbonate structure into the urethane resin
- Polycarbonate polyol can be synthesized using an alkanediol and a carbonic acid diester as raw materials under an ester exchange catalyst.
- alkanediols include 1,6-hexanediol, 1,5-pentanediol, 1,4-butanediol, and 2-methyl-1,3-propanediol.
- Polycarbonate polyol can form a coating with excellent mechanical strength and elongation properties.
- One type of polyol may be used alone, or two or more types may be used in combination.
- the number average molecular weight (Mn) of the polycarbonate polyol is preferably 500 or more, more preferably 600 or more, even more preferably 700 or more, and is preferably 10,000 or less, more preferably 8,000 or less, and even more preferably 5,000 or less, from the viewpoint of the mechanical strength and elongation properties of the coating. Any combination of these lower limit values and upper limit values may be used.
- the number average molecular weight of the polycarbonate polyol is preferably 500 to 10,000, more preferably 600 to 8,000, and even more preferably 700 to 5,000. If Mn is 500 or more, a coating with excellent mechanical strength can be formed. If Mn is 10,000 or less, a coating with excellent elongation properties can be formed.
- the polyol may contain a low molecular weight polyol as a chain extender.
- the low molecular weight polyol increases the molecular weight of the urethane resin and can further increase the mechanical strength of the coating.
- Examples of low molecular weight polyols include ethylene glycol, 1,3-propanediol, 1,4-butanediol, 1,5-pentanediol, 1,6-hexanediol, neopentyl glycol, 1,10-decanediol, 1,1-cyclohexanedimethanol, 1,4-cyclohexanedimethanol, tricyclodecanedimethanol, xylylene glycol, bis(p-hydroxy)diphenyl, bis(p-hydroxyphenyl)propane, 2,2-bis[4-(2-hydroxyethoxy)phenyl]propane, bis[4-(2-hydroxyethoxy)phenyl]sulfone, and 1,
- the amount of polyisocyanate used can be designed based on the molar ratio of the hydroxyl groups of the polyol to the isocyanato groups of the polyisocyanate (OH [mol]/NCO [mol]).
- the molar ratio is preferably 0.5 or more.
- the molar ratio is preferably 0.9 or less, more preferably 0.8 or less, and even more preferably 0.7 or less. Any combination of these lower and upper limits is acceptable.
- the molar ratio is preferably 0.5 to 0.9, more preferably 0.5 to 0.8, and even more preferably 0.5 to 0.7. If the molar ratio is 0.9 or less, the mechanical strength of the coating can be increased. If the molar ratio is 0.5 or more, the elongation properties of the coating can be increased.
- the molar ratio of the hydroxyl groups of the polycarbonate polyol to the isocyanato groups of the polyisocyanate is preferably 0.5 or more.
- the molar ratio is preferably 0.9 or less, more preferably 0.8 or less, and even more preferably 0.7 or less. Any combination of these lower and upper limits may be used.
- the molar ratio is preferably 0.5 to 0.9, more preferably 0.5 to 0.8, and even more preferably 0.5 to 0.7.
- the reaction temperature for the polyaddition reaction is not particularly limited, but is preferably 20°C to 200°C, more preferably 50°C to 150°C, and even more preferably 80°C to 120°C.
- the polyaddition reaction may be carried out using a catalyst.
- catalysts include amine compounds such as triethylamine, N-ethylmorpholine, triethylenediamine, and diazabicycloundecene; organotin compounds such as trimethyltin laurate and dibutyltin dilaurate; organotitanium compounds; and organolead compounds such as lead octylate.
- a single catalyst may be used alone, or two or more catalysts may be used in combination.
- the polyaddition reaction may be carried out substantially in the absence of a solvent, or in the presence of a solvent.
- a solvent examples include dimethylformamide, diethylformamide, dimethylacetamide, dimethylsulfoxide, tetrahydrofuran, methyl isobutyl ketone, dioxane, cyclohexanone, benzene, toluene, and ethyl cellosolve.
- the solvent may be used alone or in combination of two or more.
- the urethane resin is a urethane (meth)acrylate resin.
- the urethane (meth)acrylate resin can form a coating with high mechanical strength by heat curing.
- a resin obtained by introducing a (meth)acryloyl group into the terminal hydroxyl group or isocyanato group of the urethane resin obtained by reacting the polyisocyanate with the polyalcohol can be used.
- the urethane (meth)acrylate resin may be used alone or in combination of two or more types.
- a method of reacting a terminal isocyanato group with a hydroxyl group-containing (meth)acrylic compound for example, a method of reacting a terminal hydroxyl group with an isocyanato group-containing (meth)acrylic compound can be used.
- the hydroxyl group-containing (meth)acrylic compound and the isocyanato group-containing (meth)acrylic compound may each be used alone or in combination of two or more kinds.
- hydroxyl group-containing (meth)acrylic compounds examples include 2-hydroxyethyl (meth)acrylate, 2-hydroxypropyl (meth)acrylate, 3-hydroxybutyl (meth)acrylate, 4-hydroxybutyl (meth)acrylate, caprolactone-modified hydroxyalkyl (meth)acrylate, polyethylene glycol mono(meth)acrylate, polypropylene glycol mono(meth)acrylate, tris(hydroxyethyl)isocyanuric acid di(meth)acrylate, pentaerythritol tri(meth)acrylate, glycerin mono(meth)acrylate, and hydroxyethylacrylamide, with 2-hydroxyethyl (meth)acrylate, 2-hydroxypropyl (meth)acrylate, caprolactone-modified hydroxyalkyl (meth)acrylate, and hydroxyethylacrylamide being preferred.
- isocyanato group-containing (meth)acrylic compounds examples include 2-(meth)acryloyloxyethyl isocyanate, 2-(meth)acryloyloxypropyl isocyanate, and 1,1-bis(acryloyloxymethyl)ethyl isocyanate.
- the unreacted hydroxyl group-containing (meth)acrylic compound or the unreacted isocyanato group-containing (meth)acrylic compound can be used as an ethylenically unsaturated monomer, which will be described later.
- the number average molecular weight (Mn) of the urethane resin is preferably 500 or more, more preferably 700 or more, even more preferably 1,000 or more, and is preferably 30,000 or less, more preferably 25,000 or less, even more preferably 20,000 or less. Any combination of these lower and upper limits may be used.
- the number average molecular weight of the urethane resin is preferably 500 to 30,000, more preferably 700 to 25,000, and even more preferably 1,000 to 20,000. If the number average molecular weight of the urethane resin is 500 to 30,000, the mechanical strength and erosion resistance of the coating will be better.
- the protective coating composition preferably contains 10% by mass or more of urethane resin, more preferably 20% by mass or more, and even more preferably 30% by mass or more.
- the protective coating composition preferably contains 90% by mass or less of urethane resin, more preferably 80% by mass or less, and even more preferably 70% by mass or less. Any combination of these lower limit values and upper limit values may be used.
- the protective coating composition preferably contains 10% by mass to 90% by mass of urethane resin, more preferably 20% by mass to 80% by mass, and even more preferably 30% by mass to 70% by mass.
- the content of the urethane resin is 10% by mass or more, the erosion resistance of the coating film is better.
- the content of the urethane resin is 90% by mass or less, the coatability of the protective coating composition is good.
- the content of the urethane resin is calculated as a solid content.
- the protective coating composition of one embodiment further comprises an epoxy (meth)acrylate resin.
- the epoxy (meth)acrylate resin is generally a compound having an ethylenically unsaturated bond obtained by ring-opening reaction between an epoxy group of an epoxy compound having two or more epoxy groups and a carboxy group of an unsaturated monobasic acid having an ethylenically unsaturated bond and a carboxy group.
- the epoxy (meth)acrylate resin may be used alone or in combination of two or more kinds.
- the epoxy compound is not particularly limited as long as it has two or more epoxy groups.
- the epoxy compound for example, at least one selected from bisphenol type epoxy compounds, hydrogenated bisphenol type epoxy compounds, and novolac phenol type epoxy compounds can be used. These epoxy compounds can further improve the mechanical strength and erosion resistance of the coating.
- Bisphenol type epoxy compounds include, for example, those obtained by reacting a bisphenol compound such as bisphenol A, bisphenol F, bisphenol S, or tetrabromobisphenol A with epichlorohydrin or methylepichlorohydrin, and those obtained by reacting one or more glycidyl ethers of the above bisphenol compounds, one or more condensates of the above bisphenol compounds, and epichlorohydrin or methylepichlorohydrin.
- a bisphenol compound such as bisphenol A, bisphenol F, bisphenol S, or tetrabromobisphenol A
- epichlorohydrin or methylepichlorohydrin epichlorohydrin or methylepichlorohydrin
- hydrogenated bisphenol type epoxy compounds include those obtained by reacting hydrogenated bisphenol with epichlorohydrin or methylepichlorohydrin, and those obtained by reacting glycidyl ether of hydrogenated bisphenol A with bisphenol compounds such as bisphenol A, bisphenol F, bisphenol S, and tetrabromobisphenol A.
- Novolak phenol type epoxy compounds include, for example, those obtained by reacting phenol novolak or cresol novolak with epichlorohydrin or methyl epichlorohydrin.
- the epoxy compound is at least one selected from the group consisting of bisphenol A type epoxy resins and hydrogenated bisphenol A type epoxy resins.
- the unsaturated monobasic acid there are no particular limitations on the unsaturated monobasic acid, so long as it is a monocarboxylic acid having an ethylenically unsaturated bond.
- unsaturated monobasic acids include (meth)acrylic acid, crotonic acid, and cinnamic acid. From the viewpoint of the mechanical strength and erosion resistance of the coating, the unsaturated monobasic acid is more preferably (meth)acrylic acid, and from the viewpoint of the mechanical strength of the coating, methacrylic acid is more preferable.
- the amount of unsaturated monobasic acid used is preferably 0.3 to 1.5 moles, more preferably 0.4 to 1.2 moles, and particularly preferably 0.5 to 1.0 moles, of the total amount of carboxyl groups in the unsaturated monobasic acid per mole of the total amount of epoxy groups in the epoxy compound. If the amount of unsaturated monobasic acid used is within the above range, a coating with high hardness can be obtained.
- Epoxy (meth)acrylate resins can be synthesized by known synthesis methods. For example, an example is a method in which an epoxy compound and an unsaturated monobasic acid are dissolved in a solvent as necessary in the presence of an esterification catalyst, and reacted at 70 to 150°C, preferably 80 to 140°C, and more preferably 90 to 130°C.
- Esterification catalysts include, for example, tertiary amines such as triethylamine, N,N-dimethylbenzylamine, N,N-dimethylaniline, 2,4,6-tris(dimethylaminomethyl)phenol, and diazabicyclooctane; phosphorus compounds such as triphenylphosphine and benzyltriphenylphosphonium chloride; and diethylamine hydrochloride.
- the esterification catalysts may be used alone or in combination of two or more.
- the unreacted unsaturated monobasic acid remaining after synthesis of the epoxy (meth)acrylate resin can be used as an ethylenically unsaturated monomer, as described below.
- the number average molecular weight (Mn) of the epoxy (meth)acrylate resin is not particularly limited, but is preferably 500 to 30,000, more preferably 700 to 25,000, and even more preferably 1,000 to 20,000. If the number average molecular weight of the epoxy (meth)acrylate resin is 500 to 30,000, the mechanical strength and erosion resistance of the coating will be better.
- the protective coating composition contains 1% to 80% by weight, preferably 3% to 70% by weight, and more preferably 5% to 60% by weight of an epoxy (meth)acrylate resin.
- an epoxy (meth)acrylate resin When the epoxy (meth)acrylate resin content is 1% by weight or more, the mechanical strength of the coating can be increased. When the epoxy (meth)acrylate resin content is 80% by weight or less, the elongation properties of the coating can be increased.
- the epoxy (meth)acrylate resin content is calculated as solid content.
- the protective coating composition includes an ethylenically unsaturated monomer as a diluent monomer.
- the diluent monomer can adjust the viscosity of the protective coating composition to improve workability and coatability.
- the diluent monomer may be used alone or in combination of two or more.
- ethylenically unsaturated monomers include vinyl compounds such as styrene, vinyltoluene, t-butylstyrene, methoxystyrene, divinylbenzene, vinylnaphthalene, and acenaphthylene; diene compounds such as butadiene, 2,3-dimethylbutadiene, isoprene, and chloroprene; methyl (meth)acrylate, ethyl (meth)acrylate, propyl (meth)acrylate, n-butyl (meth)acrylate, t-butyl (meth)acrylate, and 2-ethylhexyl (meth)acrylate.
- vinyl compounds such as styrene, vinyltoluene, t-butylstyrene, methoxystyrene, divinylbenzene, vinylnaphthalene, and acenaphthylene
- acrylate isodecyl (meth)acrylate, lauryl (meth)acrylate, tridecyl (meth)acrylate, stearyl (meth)acrylate, cyclohexyl (meth)acrylate, furfuryl (meth)acrylate, tetrahydrofurfuryl (meth)acrylate, phenyl (meth)acrylate, benzyl (meth)acrylate, phenoxyethyl (meth)acrylate, dicyclopentenyl (meth)acrylate, dicyclopentenyloxyethyl (meth)acrylate (meth)acrylate compounds such as acrylate, allyl (meth)acrylate, isobornyl (meth)acrylate, ethylene glycol di(meth)acrylate, diethylene glycol di(meth)acrylate, propylene glycol di(meth)acrylate, neopentyl glycol di(meth)acrylate, tricyclodecano
- the ethylenically unsaturated monomer is preferably at least one selected from the group consisting of styrene, vinyl toluene, methyl (meth)acrylate, ethyl (meth)acrylate, propyl (meth)acrylate, t-butyl (meth)acrylate, phenyl (meth)acrylate, isobornyl (meth)acrylate, and benzyl (meth)acrylate, and more preferably at least one selected from the group consisting of styrene, vinyl toluene, t-butyl methacrylate, and isobornyl acrylate.
- the content of the ethylenically unsaturated monomer is preferably 10% to 95% by mass, more preferably 30% to 90% by mass, and even more preferably 50% to 80% by mass, based on the total of the urethane resin, the epoxy (meth)acrylate resin, and the ethylenically unsaturated monomer. If the content of the ethylenically unsaturated monomer is within the above range, the mechanical strength of the coating can be further increased.
- the protective coating composition may contain a radical polymerization initiator as a curing agent to promote curing.
- a radical polymerization initiator When the radical polymerization initiator is added to the protective coating composition, the curing of the protective coating composition is initiated. Therefore, for example, when the protective coating composition is stored, it is desirable to add the radical polymerization initiator to the protective coating composition immediately before the curing of the protective coating composition.
- the curing agent When the protective coating composition is stored under conditions in which the radical polymerization reaction does not start, the curing agent may be included in the protective coating composition in advance from the viewpoint of work efficiency.
- the curing agent may be used alone or in combination of two or more kinds.
- the radical polymerization initiator can be appropriately selected depending on the application, curing conditions, etc., and is not particularly limited.
- radical polymerization initiators include thermal radical initiators and photoradical initiators, with thermal radical initiators being preferred from the viewpoint of workability.
- thermal radical initiators include organic peroxides such as diacyl peroxides, such as benzoyl peroxide; peroxy esters, such as t-butyl peroxybenzoate; hydroperoxides, such as cumene hydroperoxide; dialkyl peroxides, such as dicumyl peroxide; ketone peroxides, such as methyl ethyl ketone peroxide and acetylacetone peroxide; peroxy ketals, such as 1,1-dialkylperoxycyclohexane; alkyl peresters, such as alkyl peroxydecanoate; and percarbonates, such as peroxydicarbonate.
- organic peroxides such as diacyl peroxides, such as benzoyl peroxide; peroxy esters, such as t-butyl peroxybenzoate; hydroperoxides, such as cumene hydroperoxide; dialkyl peroxides, such as dicumyl peroxide;
- the amount of radical polymerization initiator used is preferably 0.1 to 10 parts by mass, more preferably 0.5 to 8 parts by mass, and even more preferably 0.5 to 5 parts by mass, per 100 parts by mass of the total of the urethane resin, the epoxy (meth)acrylate resin, and the ethylenically unsaturated monomer. If the content of the radical polymerization initiator is 0.1 parts by mass or more, the curing of the protective coating composition can be rapidly promoted. If the content of the radical polymerization initiator is 10 parts by mass or less, a good balance between productivity and cost is achieved.
- the protective coating composition may contain a curing accelerator to accelerate the radical polymerization reaction of the protective coating composition.
- the curing accelerator may be used alone or in combination of two or more.
- Examples of the curing accelerator include salts of metal elements and organic acids.
- Examples of the metal elements include cobalt, vanadium, and manganese.
- Specific examples of the curing accelerator include manganese octoate, cobalt octoate, zinc octoate, vanadium octoate, cobalt naphthenate, copper naphthenate, barium naphthenate, vanadium acetoacetate, cobalt acetoacetate, and iron acetoacetate.
- manganese octoate, cobalt octoate, and cobalt naphthenate are preferred.
- the amount of the curing accelerator used is preferably 0.01 to 6.0 parts by mass, more preferably 0.02 to 4.0 parts by mass, and even more preferably 0.03 to 3.0 parts by mass, per 100 parts by mass of the total of the urethane resin, epoxy (meth)acrylate resin, and ethylenically unsaturated monomer.
- the amount of the curing accelerator used within the above range, the radical polymerization reaction of the protective coating composition can be rapidly promoted at low to room temperature, for example, in the temperature range of 5°C to 40°C.
- the protective coating composition may contain a solvent.
- the solvent may be derived from the solvent used in the synthesis of the urethane resin or the epoxy (meth)acrylate resin.
- the solvent include esters such as n-butyl acetate and n-propyl acetate; and aromatic hydrocarbons such as benzene, toluene, and xylene.
- the solvent does not include the diluting monomer.
- the content of the solvent can be appropriately determined depending on the application and the application method. For example, the content of the solvent can be set so that the solid content of the protective coating composition is 10% by mass to 90% by mass, 20% by mass to 80% by mass, or 30% by mass to 70% by mass.
- the protective coating composition may further comprise additives, such as dispersants, fillers, thixotropic agents, thixotropic aids, colorants, and polymerization inhibitors.
- additives such as dispersants, fillers, thixotropic agents, thixotropic aids, colorants, and polymerization inhibitors.
- DISPERBYK-2152 manufactured by BYK Japan Co., Ltd.
- fillers examples include calcium carbonate, aluminum hydroxide, fly ash, barium sulfate, talc, clay, glass flakes, glass powder, and wood flour.
- Hollow fillers such as glass microballoons, saran resin microballoons, acrylonitrile microballoons, and shirasu balloons can also be used as fillers.
- Thixotropic agents include, for example, inorganic powders such as silica and clay.
- the thixotropic agent can adjust the rheological properties of the protective coating composition to improve its applicability.
- the protective coating composition contains particles such as fillers and pigments, the thixotropic agent can also suppress the settling of these particles to improve the storage stability of the protective coating composition.
- thixotropy-imparting aids examples include polyethylene glycol, glycerin, polyhydroxycarboxylic acid amide, organic quaternary ammonium salts, and BYK-R-605 (manufactured by BYK Japan Co., Ltd.).
- Colorants include, for example, organic pigments, inorganic pigments such as titanium oxide, and dyes.
- polymerization inhibitors examples include hydroquinone, trimethylhydroquinone, p-benzoquinone, naphthoquinone, tert-butylhydroquinone, catechol, p-tert-butylcatechol, and 2,6-di-tert-butyl-4-methylphenol.
- additives include, for example, defoamers, UV absorbers, light stabilizers, thickeners, and plasticizers.
- the viscosity of the protective coating composition is preferably 10 mPa ⁇ s to 20,000 mPa ⁇ s, more preferably 50 mPa ⁇ s to 15,000 mPa ⁇ s, and even more preferably 100 mPa ⁇ s to 10,000 mPa ⁇ s.
- the viscosity of the protective coating composition is defined as the shear viscosity at 25°C and a rotation speed of 100 rpm using a cone and plate viscometer in accordance with JIS K 5600-2-3:2014.
- the protective coating composition is applied to at least a portion of the mold surface to form a film.
- FIG. 2(a) shows a cross-sectional view of a mold 20.
- the mold 20 has a mold surface 22 and includes an internal heater 24 for heating the stack during the heating process.
- the mold 20 in FIG. 2 is shown forming a portion of a wind power blade.
- a protective coating composition is applied to a portion of the mold surface 22 to form a coating 12.
- the coating 12 is formed on a portion of the mold surface 22 that corresponds to the leading edge of the wind power blade.
- the protective coating composition can be applied to the mold surface using known application means, such as a spray, brush, roll, trowel, spatula, syringe, etc.
- the coating formed by application may be pre-cured, for example, at 5°C to 40°C for 10 minutes to 72 hours.
- the thickness of the coating may vary depending on the shape of the wind power blade, the required mechanical strength, etc.
- the coating thickness on the wind power blade is 0.5 mm or more.
- the coating thickness is 2 mm or less. Any combination of these lower and upper limits may be used.
- the coating thickness is 0.5 mm to 2 mm.
- the coating is partially formed on the mold surface.
- the coating is, for example, a leading edge protection material for a wind power blade.
- the leading edge protection material in this embodiment can also be said to be a gel coat. That is, the coating functions as both a leading edge protection material and a gel coat.
- a separate coating may be formed on the mold surface other than where the coating is formed.
- the coating is a leading edge protectant and the separate coating is a gel coat used on typical wind turbine blades.
- another coating composition may be applied to cover the film and at least a portion of the mold surface to form a second coating.
- An example of the other coating composition is a gel coat agent used for typical wind power generation blades.
- a fiber-containing substrate impregnated with a matrix resin is disposed on the coating to form a stack.
- the fiber-containing substrate impregnated with a matrix resin include prepregs containing glass fibers or carbon fibers.
- the placement step may include impregnating the fiber substrate with a matrix resin on the coating to form a fiber-containing substrate.
- the impregnation may be performed, for example, using a hand lay-up method or a vacuum-assisted impregnation method.
- the fiber substrate examples include substrates containing fibers such as glass fiber, carbon fiber, polyester fiber, aramid fiber, vinylon fiber, and cellulose nanofiber.
- the fiber substrate that can be used include short fibers, long fibers, twisted yarns, chops, chopped strand mats, continuous strand mats, rovings, nonwoven fabrics, roving cloths, woven fabrics, braids, three-dimensional woven fabrics, and three-dimensional braids.
- the nonwoven fabrics include spunbond nonwoven fabrics and meltblown nonwoven fabrics. Examples of the woven fabrics include plain weaves, satin weaves, and twill weaves.
- the matrix resin can be any resin commonly used in FRP molding.
- An example of the matrix resin is a thermosetting epoxy resin.
- a method for forming a fiber-containing substrate by impregnating a fiber substrate with a matrix resin on a coating using a vacuum-assisted impregnation method will be described.
- a fiber substrate 142 is arranged to cover the coating 12 and the mold surface 22.
- a sheet 26 is arranged on the fiber substrate 142 to make the space between the sheet 26 and the mold surface 22 airtight.
- An exhaust port 28 is provided at one end of the sheet 26. The exhaust port 28 is connected to a vacuum pump, and the space between the sheet 26 and the mold surface 22 can be placed under reduced pressure by operating the vacuum pump.
- a matrix resin supplying device 30 that contains a matrix resin 144 inside is installed at the other end of the sheet.
- the matrix resin 144 is impregnated into the fiber substrate 142 by opening a valve 32 and operating the vacuum pump to reduce the pressure in the space between the sheet 26 and the mold surface 22, thereby forming a fiber-containing substrate 14 on the coating 12.
- the fiber-containing substrate 14 combines with the coating 12 to form a stack 16.
- the stack is heated to form a molded article in which the coating and the fiber-containing substrate are bonded.
- the coating includes a cured product of the protective coating composition, i.e., a cured coating.
- the cured coating is more firmly bonded to the fiber-containing substrate, and therefore a molded article having better erosion resistance can be obtained.
- the heater 24 is operated to heat the stack 16. This forms the wind power generation blade 10 shown in FIG. 1, in which the coating 12 and the fiber-containing substrate 14 are bonded together.
- the heating temperature can be, for example, 50°C to 200°C.
- the heating time can be, for example, 30 minutes to 24 hours.
- the fiber-containing substrate is a prepreg, for example, autoclave molding or press molding can be used.
- the coating is disposed at least on the tip of the leading edge of the wind power blade.
- the tip of the leading edge refers to, for example, a portion of the leading edge that extends from the end furthest from the axis of rotation of the wind power blade by 1% to 50%, 5% to 40%, or 10% to 30% of the blade length of the wind power blade.
- the coating functions as a leading edge protective material. This embodiment is suitable for large wind power blades, whose tip portions move at high speeds and are therefore prone to erosion.
- the coating can be disposed on the entire leading edge, including the tip, or on the entire surface of the wind power blade.
- the blade length of the wind power blade is preferably 10 m or more, more preferably 20 m or more, and even more preferably 30 m or more.
- the blade length of the wind power blade can be, for example, 140 m or less, 100 m or less, or 80 m or less. Any combination of these lower and upper limits may be used. In one embodiment, the blade length of the wind power blade is 10 m to 140 m, 20 m to 100 m, or 30 m to 80 m.
- the protective coating composition of the present disclosure can be suitably used to form leading edge protective materials for wind power blades.
- the protective coating composition of the present disclosure can be suitably used for a variety of applications where erosion resistance is desired, such as propellers for airplanes, fins for coolers, vehicle components for high-speed trains, pipes for chemical plants, chemical storage tanks, and concrete repair materials.
- the viscosity of the protective coating composition was evaluated by the following procedure: The shear viscosity was measured at 25° C. and a rotation speed of 100 rpm using a cone-plate viscometer (RE-215U, manufactured by Toki Sangyo Co., Ltd., rotor: 1°34′ ⁇ R24) in accordance with JIS K 5600-2-3:2014 “General test methods for paints-Part 2: Properties and stability of paints-Section 3: Viscosity (cone-plate viscometer method).”
- a test piece 50 mm ⁇ 80 mm ⁇ 2 mm (thickness) was placed in a thermo-hygrostat (PL-2J, manufactured by Espec Corporation) and subjected to 100 cycles of repeated heat and humidity cycles at ⁇ 40° C. for 6 hours and at 60° C. and 98% relative humidity for 6 hours. After that, the appearance was visually inspected for the presence or absence of chalking, blisters, and cracks. A: None of chalking, blisters, or cracks occurred. B: No cracks occurred, and neither chalking nor blisters occurred. C: No cracks occurred. D: Cracks occurred.
- Urethane (meth)acrylate resin and epoxy (meth)acrylate resin were synthesized using the following procedure.
- the protective coating composition was prepared as follows:
- Example 1 40 g of the urethane (meth)acrylate resin UAc-1 obtained in Synthesis Example 1 above, 60 g of vinyl toluene, 0.5 g of 8% cobalt octylate, and 1.5 g of curing agent 328E were added and stirred at 2000 rpm for 1 minute using a planetary centrifugal mixer, to obtain a protective coating composition of Example 1.
- the protective coating composition was poured into a silicone mold 2 mm deep and left for 3 hours at 23°C for pre-curing and 6 hours at 70°C for post-curing to obtain a molded product of the protective coating composition.
- Pre-curing corresponds to the process of applying the protective coating composition to the mold surface to form a coating
- post-curing corresponds to the process of heating the stack of the coating and the fiber-containing substrate.
- Table 3 The evaluation results of the protective coating composition and the molded product are shown in Table 3.
- Examples 2 to 15, Comparative Examples 1 to 4 A protective coating composition was obtained in the same manner as in Example 1, except that the raw materials and their amounts were as shown in Table 3.
- a molded article was obtained from the obtained protective coating composition in the same manner as in Example 1. The evaluation results of the protective coating composition and the molded article are shown in Table 3.
- Example 16 A molded article was obtained in the same manner as in Example 1, except that the protective coating composition of Example 1 was poured into a silicone mold having a depth of 0.1 mm. The evaluation results of the molded article are shown in Table 3.
- the protective coating composition disclosed herein can be suitably used to manufacture leading edge protection materials for wind power blades.
Landscapes
- Chemical & Material Sciences (AREA)
- Organic Chemistry (AREA)
- Life Sciences & Earth Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Wood Science & Technology (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Paints Or Removers (AREA)
Abstract
Description
同一分子内にウレタン構造及びカーボネート構造を有するウレタン樹脂、及び
エチレン性不飽和化合物
を含む保護コーティング組成物であって、
前記ウレタン樹脂が、ウレタン(メタ)アクリレート樹脂であり、
前記保護コーティング組成物の硬化物の耐エロージョン性が1.5時間以上である、保護コーティング組成物。
[態様2]
エポキシ(メタ)アクリレート樹脂を更に含む、態様1に記載の保護コーティング組成物。
[態様3]
前記ウレタン樹脂を10質量%~90質量%含む、態様1又は2に記載の保護コーティング組成物。
[態様4]
前記ウレタン樹脂が、ポリカーボネートポリオール及びポリイソシアネートを含む組成物の反応生成物であり、前記ポリカーボネートポリオールの水酸基と前記ポリイソシアネートのイソシアナト基とのモル比(OH[mol]/NCO[mol])が0.5~0.9である、態様1~3のいずれか一項に記載の保護コーティング組成物。
[態様5]
前記ポリカーボネートポリオールの数平均分子量が500~10,000である、態様4に記載の保護コーティング組成物。
[態様6]
前記ポリイソシアネートが脂環式ポリイソシアネートを含む、態様4又は5に記載の保護コーティング組成物。
[態様7]
前記ウレタン樹脂の数平均分子量が500~30,000である、態様1~6のいずれか一項に記載の保護コーティング組成物。
[態様8]
前記保護コーティング組成物が、風力発電ブレードのリーディングエッジ保護剤である、態様1~7のいずれか一項に記載の保護コーティング組成物。
[態様9]
前記風力発電ブレードのブレード長が10m以上である、態様8に記載の保護コーティング組成物。
装置:Shodex(商標) GPC-101(株式会社レゾナック)
カラム:Shodex(商標) LF-804(株式会社レゾナック)
カラム温度:40℃
試料:試料の0.2質量%テトラヒドロフラン溶液
流量:1mL/分
溶離液:テトラヒドロフラン
検出器:Shodex(商標) RI-71S(株式会社レゾナック)
一実施形態では、同一分子内にウレタン構造及びカーボネート構造を有するウレタン樹脂、及びエチレン性不飽和化合物を含む保護コーティング組成物が提供される。この実施形態において、ウレタン樹脂はウレタン(メタ)アクリレート樹脂であり、保護コーティング組成物の硬化物の耐エロージョン性は1.5時間以上である。耐エロージョン性は、保護コーティング組成物の硬化物を厚さ2mmの被膜として形成し、実施例に記載の手順に従って評価したときの値である。保護コーティング組成物の硬化物の耐エロージョン性は、好ましくは0.5時間以上、より好ましくは1.0時間以上、更に好ましくは1.5時間以上である。
一実施形態の保護コーティング組成物は、同一分子内にウレタン構造及びカーボネート構造を有するウレタン樹脂を含む。同一分子内にウレタン構造及びカーボネート構造を有するウレタン樹脂は、高い機械強度と優れた伸び特性を併せ持つ。ウレタン樹脂のこれらの特性は、保護コーティング組成物の硬化物の優れた耐エロージョン性に寄与する。
同一分子内にウレタン構造及びカーボネート構造を有するウレタン樹脂は、少なくとも、ポリイソシアネートと、ポリオールとを重付加反応させて得ることができ、ポリイソシアネート及びポリオールの少なくとも一方にカーボネート構造を有する。ウレタン樹脂は、一種を単独で用いてもよいし、二種以上を併用してもよい。
一実施形態の保護コーティング組成物は、エポキシ(メタ)アクリレート樹脂を更に含む。エポキシ(メタ)アクリレート樹脂は、一般には、2個以上のエポキシ基を有するエポキシ化合物のエポキシ基と、エチレン性不飽和結合及びカルボキシ基を有する不飽和一塩基酸のカルボキシ基との開環反応によって得られる、エチレン性不飽和結合を有する化合物である。エポキシ(メタ)アクリレート樹脂は、一種を単独で使用してもよいし、二種以上を併用してもよい。
保護コーティング組成物は、希釈性モノマーとしてエチレン性不飽和単量体を含む。希釈性モノマーは、保護コーティング組成物の粘度を調整して、作業性及び塗工性を高めることができる。希釈性モノマーは、一種を単独で用いてもよいし、二種以上を併用してもよい。
保護コーティング組成物は、硬化を促進させるために、硬化剤としてラジカル重合開始剤を含んでもよい。保護コーティング組成物にラジカル重合開始剤を添加すると、保護コーティング組成物の硬化が開始する。そのため、例えば、保護コーティング組成物を貯蔵する場合には、ラジカル重合開始剤を保護コーティング組成物の硬化直前に保護コーティング組成物中に添加することが望ましい。ラジカル重合反応が開始しない条件下で保護コーティング組成物が貯蔵される場合は、作業効率の観点から、硬化剤を保護コーティング組成物中に予め含有させておくこともできる。硬化剤は、一種を単独で用いてもよいし、二種以上を併用してもよい。
保護コーティング組成物は、保護コーティング組成物のラジカル重合反応を促進させるために、硬化促進剤を含んでもよい。硬化促進剤は、一種を単独で用いてもよいし、二種以上を併用してもよい。
保護コーティング組成物は、溶剤を含んでもよい。溶剤は、ウレタン樹脂又はエポキシ(メタ)アクリレート樹脂の合成の際に使用した溶剤に由来してもよい。溶剤としては、例えば、酢酸n-ブチル、酢酸n-プロピル等のエステル;及びベンゼン、トルエン、キシレン等の芳香族炭化水素が挙げられる。本開示において、溶剤には前記希釈モノマーは含まれない。溶剤の含有量は、用途及び塗布方法に応じて適宜決定することができる。例えば、溶剤の含有量は、保護コーティング組成物の固形分が、10質量%~90質量%、20質量%~80質量%、又は30質量%~70質量%となるように設定することができる。
保護コーティング組成物は、添加剤を更に含んでもよい。添加剤としては、例えば、分散剤、充填材、揺変剤、揺変性付与助剤、着色剤、及び重合禁止剤が挙げられる。
保護コーティング組成物の粘度は、好ましくは10mPa・s~20,000mPa・s、より好ましくは50mPa・s~15,000mPa・s、更に好ましくは100mPa・s~10,000mPa・sである。保護コーティング組成物の粘度を上記範囲とすることにより、作業性及び塗工性を高めることができる。本開示において、保護コーティング組成物の粘度は、JIS K 5600-2-3:2014に準拠し、コーン・プレート粘度計を用いて25℃、回転速度100rpmにおけるずり粘度として定義される。
塗布工程では、前記保護コーティング組成物を金型表面の少なくとも一部に塗布して、被膜を形成する。
配置工程では、マトリクス樹脂が含浸された繊維含有基材を被膜上に配置して、スタックを形成する。マトリクス樹脂が含浸された繊維含有基材としては、例えば、ガラス繊維又は炭素繊維を含むプリプレグが挙げられる。
加熱工程では、スタックを加熱して、被膜と繊維含有基材とが接合された成形物を形成する。被膜は、保護コーティング組成物の硬化物を含む、すなわち硬化被膜である。硬化被膜は、繊維含有基材とより強固に接合するため、耐エロージョン性により優れた成形物を得ることができる。
保護コーティング組成物の粘度を以下の手順で評価した。JIS K 5600-2-3:2014「塗料一般試験方法-第2部:塗料の性状・安定性-第3節:粘度(コーン・プレート粘度計法)」に準拠し、コーン・プレート粘度計(RE-215U、東機産業株式会社製、ロータ:1°34’×R24)を用いて25℃、回転速度100rpmにおけるずり粘度を測定した。
高圧洗浄機(SH-0807、スーパー工業株式会社製)を用いて水圧6.0MPa、水量6L/min、試験片-ノズル間距離7cmとして、50mm×60mm×2mm(厚さ)の試験片に対して23℃で30分間連続して水流を直撃させた後、試験片の損傷の有無を目視にて確認した。損傷するまでに要した時間を耐エロージョン性とした。
JIS K 5600-5-7:2014「塗料一般試験方法-第5部:塗膜の機械的性質-第7節:付着性(プルオフ法)」に準拠し、標準ガラスエポキシ板(60mm×150mm×2mm(厚さ)、日本テストパネル株式会社製)上に厚さ0.5mmで被膜を形成し、ドリー(直径20mm、アルミニウム製)を接着剤(メタルロック(商標)、セメダイン株式会社製)を用いて被膜に固着させた後、接着強度をアドヒージョンテスター(ポジテストAT-A、COTEC株式会社製)を用いて測定した。接着強度はN=3で測定した平均値として定義した。
試験片(50mm×80mm×2mm(厚さ))を恒温恒湿槽(PL-2J、エスペック株式会社製)内に静置し、-40℃で6時間、60℃相対湿度98%で6時間の繰り返し湿熱サイクル条件で100サイクル経過した後、外観のチョーキング、ブリスター及びクラックの有無を目視にて確認した。
A:チョーキング、ブリスター及びクラックのいずれもなかった
B:クラックはなかった、チョーキング及びブリスターいずれか一方はなかった
C:クラックはなかった
D:クラックが発生した
乾式シリカ レオロシールPM-20L(株式会社トクヤマ製)
酸化チタン PFC-105(石原産業株式会社製)
ガラスパウダー CF0033(タカラスタンダード株式会社製)
ガラスフレーク(商標) RCF-160N(日本板硝子株式会社製)
DISPERBYK-2152(BYKジャパン株式会社製)
8%オクチル酸コバルト(ヘキソエートコバルト8%、東栄化工株式会社製)
硬化剤328E(t-ブチルパーオキシベンゾエート、クメンハイドロパーオキサイド混合物、化薬ヌーリオン株式会社製)
パークミル(商標) H-80(クメンハイドロパーオキサイド、日油株式会社製)
撹拌機、還流冷却管、温度計、及びガス導入管を備えたフラスコに、4,4’-メチレンビスシクロへキシルジイソシアネート(デスモジュールW、住化コベストロウレタン株式会社製)142g、ポリカーボネートジオール(ETERNACOLL PH-100、UBE株式会社製)411g、及びジブチルスズジラウレート0.4gを仕込み、加熱撹拌しながら80℃にて4時間反応させた。その後、2-ヒドロキシエチルメタクリレート46gを仕込み、乾燥空気を吹き込み加熱撹拌しながら80℃で4時間反応させ、ウレタン(メタ)アクリレート樹脂UAc-1を得た。
原料及びそれらの配合量を表2に記載のとおりとした以外は、合成例1と同じ手順でウレタン(メタ)アクリレート樹脂UAc-2~UAc-7を得た。
撹拌機、還流冷却管、温度計、及びガス導入管を備えたフラスコに、ビスフェノールA型エポキシ樹脂(エポミックR140、三井化学ファイン株式会社製)683g、メタクリル酸313g、トリエチルアミン3.0g、ハイドロキノン0.6gを仕込み、空気を吹き込みながら120℃で反応させ、酸価が5mgKOH/g以下になった時点で冷却して、エポキシ(メタ)アクリレート樹脂EAc-1を得た。
原料及びそれらの配合量を表2に記載のとおりとした以外は、合成例8と同じ手順でエポキシ(メタ)アクリレート樹脂EAc-2を得た。
上記合成例1で得られたウレタン(メタ)アクリレート樹脂UAc-1 40g、ビニルトルエン60g、8%オクチル酸コバルト0.5g、硬化剤328E 1.5gを加え、自転公転ミキサーを用いて2000rpmにて1分間撹拌することで、例1の保護コーティング組成物を得た。
原料及びそれらの配合量を表3に記載のとおりとした以外は、例1と同じ手順で保護コーティング組成物を得た。得られた保護コーティング組成物から例1と同じ手順で成形品を得た。保護コーティング組成物及び成形品の評価結果を表3に示す。
例1の保護コーティング組成物を用いて、表3に記載の条件で前硬化のみで後硬化を行なわずに成形品を得た。成形品の評価結果を表3に示す。
例1の保護コーティング組成物を深さ0.1mmのシリコーン型内に流し入れた以外は、例1と同じ手順で成形品を得た。成形品の評価結果を表3に示す。
12 被膜
14 繊維含有基材
142 繊維基材
144 マトリクス樹脂
16 スタック
20 金型
22 金型表面
24 ヒーター
26 シート
28 排気口
30 マトリクス樹脂供給装置
32 バルブ
Claims (9)
- 同一分子内にウレタン構造及びカーボネート構造を有するウレタン樹脂、及び
エチレン性不飽和化合物
を含む保護コーティング組成物であって、
前記ウレタン樹脂が、ウレタン(メタ)アクリレート樹脂であり、
前記保護コーティング組成物の硬化物の耐エロージョン性が1.5時間以上である、保護コーティング組成物。 - エポキシ(メタ)アクリレート樹脂を更に含む、請求項1に記載の保護コーティング組成物。
- 前記ウレタン樹脂を10質量%~90質量%含む、請求項1又は2に記載の保護コーティング組成物。
- 前記ウレタン樹脂が、ポリカーボネートポリオール及びポリイソシアネートを含む組成物の反応生成物であり、前記ポリカーボネートポリオールの水酸基と前記ポリイソシアネートのイソシアナト基とのモル比(OH[mol]/NCO[mol])が0.5~0.9である、請求項1又は2に記載の保護コーティング組成物。
- 前記ポリカーボネートポリオールの数平均分子量が500~10,000である、請求項4に記載の保護コーティング組成物。
- 前記ポリイソシアネートが脂環式ポリイソシアネートを含む、請求項4に記載の保護コーティング組成物。
- 前記ウレタン樹脂の数平均分子量が500~30,000である、請求項1又は2に記載の保護コーティング組成物。
- 前記保護コーティング組成物が、風力発電ブレードのリーディングエッジ保護剤である、請求項1又は2に記載の保護コーティング組成物。
- 前記風力発電ブレードのブレード長が10m以上である、請求項8に記載の保護コーティング組成物。
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202480031743.7A CN121195032A (zh) | 2023-06-30 | 2024-06-14 | 保护涂层组合物 |
| JP2025529639A JPWO2025004844A1 (ja) | 2023-06-30 | 2024-06-14 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2023108914 | 2023-06-30 | ||
| JP2023-108914 | 2023-06-30 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2025004844A1 true WO2025004844A1 (ja) | 2025-01-02 |
Family
ID=93938908
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2024/021615 Ceased WO2025004844A1 (ja) | 2023-06-30 | 2024-06-14 | 保護コーティング組成物 |
Country Status (3)
| Country | Link |
|---|---|
| JP (1) | JPWO2025004844A1 (ja) |
| CN (1) | CN121195032A (ja) |
| WO (1) | WO2025004844A1 (ja) |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH06145276A (ja) * | 1992-11-09 | 1994-05-24 | Toagosei Chem Ind Co Ltd | 光硬化型樹脂組成物 |
| JP2002179953A (ja) * | 2000-12-13 | 2002-06-26 | Dainippon Ink & Chem Inc | プラスチック塗装用エネルギー線硬化型樹脂組成物および塗装物 |
| JP2012213998A (ja) * | 2011-03-30 | 2012-11-08 | Dainippon Printing Co Ltd | 加飾シート及びこれを用いた加飾樹脂成形品 |
| JP2013249455A (ja) * | 2012-06-04 | 2013-12-12 | Asahi Kasei Chemicals Corp | ウレタン(メタ)アクリレート及びその製造方法 |
| KR20140024562A (ko) * | 2012-08-20 | 2014-03-03 | 코오롱인더스트리 주식회사 | 하드코팅 조성물 및 이를 이용한 하드코팅 필름 |
| JP2016204627A (ja) * | 2015-04-20 | 2016-12-08 | 東洋インキScホールディングス株式会社 | 常温硬化型塗料組成物、および風力発電機のブレード |
| JP2017535625A (ja) * | 2014-12-01 | 2017-11-30 | エルジー・ケム・リミテッド | 自己復元特性を有するコーティング層形成用組成物、コーティング層およびフィルム |
| JP2020002348A (ja) * | 2018-06-21 | 2020-01-09 | 三菱ケミカル株式会社 | 活性エネルギー線硬化性樹脂組成物、およびそれを用いたコーティング剤、ならびにシート |
| JP2024057637A (ja) * | 2022-10-13 | 2024-04-25 | アイカ工業株式会社 | 光硬化性樹脂組成物、成形用ハードコートフィルム及びそれを用いた成形品 |
-
2024
- 2024-06-14 WO PCT/JP2024/021615 patent/WO2025004844A1/ja not_active Ceased
- 2024-06-14 CN CN202480031743.7A patent/CN121195032A/zh active Pending
- 2024-06-14 JP JP2025529639A patent/JPWO2025004844A1/ja active Pending
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH06145276A (ja) * | 1992-11-09 | 1994-05-24 | Toagosei Chem Ind Co Ltd | 光硬化型樹脂組成物 |
| JP2002179953A (ja) * | 2000-12-13 | 2002-06-26 | Dainippon Ink & Chem Inc | プラスチック塗装用エネルギー線硬化型樹脂組成物および塗装物 |
| JP2012213998A (ja) * | 2011-03-30 | 2012-11-08 | Dainippon Printing Co Ltd | 加飾シート及びこれを用いた加飾樹脂成形品 |
| JP2013249455A (ja) * | 2012-06-04 | 2013-12-12 | Asahi Kasei Chemicals Corp | ウレタン(メタ)アクリレート及びその製造方法 |
| KR20140024562A (ko) * | 2012-08-20 | 2014-03-03 | 코오롱인더스트리 주식회사 | 하드코팅 조성물 및 이를 이용한 하드코팅 필름 |
| JP2017535625A (ja) * | 2014-12-01 | 2017-11-30 | エルジー・ケム・リミテッド | 自己復元特性を有するコーティング層形成用組成物、コーティング層およびフィルム |
| JP2016204627A (ja) * | 2015-04-20 | 2016-12-08 | 東洋インキScホールディングス株式会社 | 常温硬化型塗料組成物、および風力発電機のブレード |
| JP2020002348A (ja) * | 2018-06-21 | 2020-01-09 | 三菱ケミカル株式会社 | 活性エネルギー線硬化性樹脂組成物、およびそれを用いたコーティング剤、ならびにシート |
| JP2024057637A (ja) * | 2022-10-13 | 2024-04-25 | アイカ工業株式会社 | 光硬化性樹脂組成物、成形用ハードコートフィルム及びそれを用いた成形品 |
Also Published As
| Publication number | Publication date |
|---|---|
| CN121195032A (zh) | 2025-12-23 |
| JPWO2025004844A1 (ja) | 2025-01-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP4856292B2 (ja) | 炭素繊維用サイジング剤、炭素繊維、及びその製造方法、ならびに、炭素繊維を含む成形材料及び成形品 | |
| TWI619737B (zh) | 碳纖維強化塑膠用樹脂組成物 | |
| CN108026300B (zh) | 预浸料和成型品 | |
| CN105778005B (zh) | 可自由基聚合的聚氨酯组合物 | |
| US5118783A (en) | Chain-stopped unsaturated polyester resins | |
| US20090076218A1 (en) | Low VOC Thermosetting Polyester Acrylic Resin for Gel Coat | |
| CN104974502A (zh) | 聚氨酯复合材料及其制备方法 | |
| JP2005247879A (ja) | 繊維強化複合材料用組成物及びその成形材料 | |
| CN115746223A (zh) | 热固树脂组合物、环氧树脂材料及其复合材料和制备方法 | |
| JP5336730B2 (ja) | 繊維強化プラスチック用ラジカル重合性接着剤を用いて接着された接着構造体及びその製造方法 | |
| CN111757899B (zh) | 对热变形和撕裂伸长率具有优异耐受性的基于聚氨酯的聚合物材料 | |
| TW202104344A (zh) | 纖維強化塑膠中間基材用液狀組成物、纖維強化塑膠中間基材及前述纖維強化塑膠中間基材之製造方法 | |
| CN1684994A (zh) | 凝胶涂料组合物 | |
| WO2017086231A1 (ja) | 繊維強化プラスチック成形品、及びその製造方法 | |
| JP2018001087A (ja) | 親水性被膜形成方法 | |
| WO2017208605A1 (ja) | プリプレグシート、及び繊維強化複合材料の製造方法 | |
| WO2014191308A1 (en) | Composite composition containing a polycyclic ether polypol | |
| JP2025007472A (ja) | 樹脂組成物の風力発電ブレードのゲルコート兼リーディングエッジ保護剤としての使用 | |
| JP2025007486A (ja) | Frp成形物の製造方法及びfrp成形物 | |
| JP5791077B2 (ja) | 成形材料及び成形品 | |
| CN121195032A (zh) | 保护涂层组合物 | |
| JP6970514B2 (ja) | ラジカル硬化性樹脂組成物、保護層及び建築施工方法 | |
| JP6626663B2 (ja) | ラジカル重合性樹脂組成物及びその硬化方法 | |
| JP6966026B2 (ja) | 繊維強化成形材料及びそれを用いた成形品 | |
| JP2004238557A (ja) | 硬化性接着剤及びそれを用いた接着方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 24831709 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2025529639 Country of ref document: JP Kind code of ref document: A |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2025529639 Country of ref document: JP |
|
| WWE | Wipo information: entry into national phase |
Ref document number: CN2024800317437 Country of ref document: CN |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |