WO2020256103A1 - 吸収性物品、及び吸収性物品の製造方法 - Google Patents
吸収性物品、及び吸収性物品の製造方法 Download PDFInfo
- Publication number
- WO2020256103A1 WO2020256103A1 PCT/JP2020/024138 JP2020024138W WO2020256103A1 WO 2020256103 A1 WO2020256103 A1 WO 2020256103A1 JP 2020024138 W JP2020024138 W JP 2020024138W WO 2020256103 A1 WO2020256103 A1 WO 2020256103A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- sheet
- absorbent article
- width direction
- dimensional
- elastic member
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images


Classifications
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/45—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape
- A61F13/49—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies
- A61F13/496—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies in the form of pants or briefs
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/15577—Apparatus or processes for manufacturing
- A61F13/15756—Applying tabs, strips, tapes, loops; Knotting the ends of pads
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/15577—Apparatus or processes for manufacturing
- A61F13/15764—Transferring, feeding or handling devices; Drives
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/15577—Apparatus or processes for manufacturing
- A61F13/15804—Plant, e.g. involving several steps
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/45—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape
- A61F13/49—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies
- A61F13/494—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies characterised by edge leakage prevention means
- A61F13/49406—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies characterised by edge leakage prevention means the edge leakage prevention means being at the crotch region
- A61F13/49413—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies characterised by edge leakage prevention means the edge leakage prevention means being at the crotch region the edge leakage prevention means being an upstanding barrier
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/15577—Apparatus or processes for manufacturing
- A61F2013/15821—Apparatus or processes for manufacturing characterized by the apparatus for manufacturing
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/45—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape
- A61F13/49—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies
- A61F13/494—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies characterised by edge leakage prevention means
- A61F2013/4948—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators characterised by the shape specially adapted to be worn around the waist, e.g. diapers or nappies characterised by edge leakage prevention means the edge leakage prevention means being elastic
Definitions
- the present invention relates to an absorbent article and a method for producing an absorbent article.
- FIG. 4 of Patent Document 1 from the side sheet 1 arranged outside the width direction of the center of the absorbent article in the width direction, the three-dimensional gathers that can stand up on the skin surface side, and the three-dimensional gathers. Also disclosed are absorbent articles having leg gathers arranged outside in the width direction. The side seats are folded back from two creases extending in the front-rear direction.
- the leg gather is configured by folding back the side sheet with one crease (outer crease in the width direction) as the base point. Since the leg gather has a contraction region that contracts in the front-rear direction with a predetermined width, it is easy to maintain the flatness of the leg gather. As a result, the leg gathers can be easily fitted to the wearer's skin on the surface, and the wearer's leg circumference can be suppressed from being locally pressed.
- the three-dimensional gather is configured by folding back the side sheet with the other crease (inner crease in the width direction) as the base point.
- the three-dimensional gather has an upright portion that can be erected by a three-dimensional elastic member having elasticity in the front-rear direction, and an upright edge that serves as an upright fulcrum of the upright portion.
- the upright portion is composed of a folded portion that is folded back from the inner crease as a base point and a non-folded portion that extends from the inner fold to the upright end edge. The end of the folded portion far from the inner crease is joined to the non-folded portion.
- the excrement that has flowed on the surface of the absorbent article and moved outward in the width direction immediately contacts the non-folded portion in the vicinity of the standing edge.
- the excrement tends to seep out of the three-dimensional gather in the width direction, and the excrement may leak.
- the fold In order to reduce the area from the edge of the fold to the rising edge, the fold extends from the inner crease to the rising edge, i.e. the length of the fold is equal to the length of the non-fold.
- the absorbent article according to one aspect is sandwiched between the front-rear direction, the width direction orthogonal to the front-rear direction, the thickness direction, the front waist circumference area, the rear waist circumference area, the front waist circumference area, and the rear waist circumference area. It has an inseam area, one side sheet arranged outside the width direction of the center of the absorbent article in the width direction, and three-dimensional gathers and leg gathers.
- the three-dimensional gather has an upright portion that can be erected by one or more three-dimensional elastic members having elasticity in the front-rear direction, and an upright edge that serves as an upright fulcrum of the upright portion.
- the leg gather has a contraction region that contracts in the front-rear direction with a predetermined width by one or more leg elastic members having elasticity in the front-rear direction, and is arranged outside the upright edge in the width direction.
- the three-dimensional gathers and the leg gathers are composed of a pair of sheet layers facing each other by folding back the side sheet 1 with one crease extending in the front-rear direction as a base point.
- the pair of sheet layers are in contact with the leg elastic member arranged on the outermost side in the width direction from the position in contact with the three-dimensional elastic member located closest to the skin surface side when the three-dimensional gather is erected. It extends continuously until.
- the method for manufacturing an absorbent article includes one side sheet arranged outside the center in the width direction of the absorbent article, three-dimensional gathers, and leg gathers, and the three-dimensional object is described.
- the gather has an upright portion that can be erected by one or more three-dimensional elastic members having elasticity in the front-rear direction, and an upright edge that serves as an upright fulcrum of the upright portion, and the leg gather has the leg gather in the front-rear direction. It has a contraction region that contracts in the front-rear direction with a predetermined width by one or more leg elastic members having elasticity, and is arranged outside the width direction from the standing edge, and is arranged with the three-dimensional gather.
- the leg gather is a method for manufacturing an absorbent article for producing an absorbent article composed of a pair of sheet layers facing each other by folding back the side sheet 1 with one crease extending in the front-rear direction as a base point.
- the manufacturing method includes a forming step in which a composite stretchable sheet having the pair of sheet layers and having elasticity forms a continuous sheet continuum in the front-rear direction.
- a plurality of continuous elastic members composed of a first continuous elastic member constituting the one or more three-dimensional elastic members and a second continuous elastic member constituting the one or more leg elastic members are formed on the side sheet of the above 1.
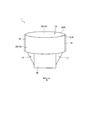
- FIG. 1 is a schematic front view of the absorbent article 1 according to the present embodiment.
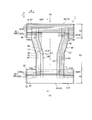
- FIG. 2 is a schematic plan view of the absorbent article 1 according to the present embodiment.
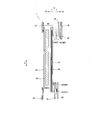
- FIG. 3 is a schematic cross-sectional view taken along the F3-F3 cross section shown in FIG.
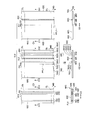
- FIG. 4 is a schematic cross-sectional view of the absorbent article shown in FIG.
- FIG. 5 is a schematic plan view of the absorbent article 1 according to the present embodiment.
- FIG. 6 is a diagram for explaining three-dimensional gathers.
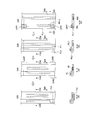
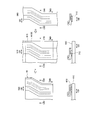
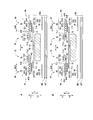
- FIG. 7 is a diagram (No. 1) for explaining a method for manufacturing the absorbent article 1.
- FIG. 8 is a diagram (No. 2) for explaining a method for manufacturing the absorbent article 1.
- FIG. 9 is a diagram (No. 3) for explaining a method for manufacturing the absorbent article 1.
- FIG. 10 is a schematic cross-sectional view of the absorbent article according to the modified example.
- the absorbent article according to one aspect is sandwiched between the front-rear direction, the width direction orthogonal to the front-rear direction, the thickness direction, the front waist circumference area, the rear waist circumference area, the front waist circumference area, and the rear waist circumference area. It has an inseam area, one side sheet arranged outside the width direction of the center of the absorbent article in the width direction, and three-dimensional gathers and leg gathers.
- the three-dimensional gather has an upright portion that can be erected by one or more three-dimensional elastic members having elasticity in the front-rear direction, and an upright edge that serves as an upright fulcrum of the upright portion.
- the leg gather has a contraction region that contracts in the front-rear direction with a predetermined width by one or more leg elastic members having elasticity in the front-rear direction, and is arranged outside the upright edge in the width direction.
- the three-dimensional gathers and the leg gathers are composed of a pair of sheet layers facing each other by folding back the side sheet 1 with one crease extending in the front-rear direction as a base point.
- the pair of sheet layers are in contact with the leg elastic member arranged on the outermost side in the width direction from the position in contact with the three-dimensional elastic member located closest to the skin surface side when the three-dimensional gather is erected. It extends continuously until.
- a pair of sheet layers are continuously present between the three-dimensional elastic member located closest to the skin surface when the three-dimensional gather is erected and the leg elastic member arranged on the outermost side in the width direction.
- the standing edge of the three-dimensional gather is present between the three-dimensional elastic member located closest to the skin surface when the three-dimensional gather stands and the leg elastic member arranged on the outermost side in the width direction, the surface of the absorbent article is affected. Even if the excrement that flows and moves outward in the width direction exudes from one sheet layer (the inner sheet layer in the width direction in the upright state and the non-skin surface side sheet layer in the extended state) to the outside in the width direction.
- the other sheet layer (the outer sheet layer in the width direction in the upright state and the sheet layer on the skin surface side in the extended state) can suppress exudation to the outside in the width direction. As a result, it is possible to suppress the leakage of excrement generated by exuding to the outside in the width direction of the three-dimensional gather.
- both of the pair of seat layers overlap all leg elastic members in the thickness direction T, which makes it easier to maintain the flatness of the leg gathers, and the leg gathers fit the wearer's skin surface. It will be easier.
- the side sheet of 1 may be folded back so that the 1 crease is arranged in the 3D gather.
- the one or more three-dimensional elastic members and the one or more leg elastic members may be sandwiched between the pair of sheet layers.
- the creases on the side sheet are softer to the touch than the edges of the side sheet (edges with cut surfaces). Therefore, when the three-dimensional gathers are erected, the folds of the side sheet, which are soft to the touch, hit the wearer's skin, so that deterioration of wearing comfort due to the erection of the three-dimensional gathers can be suppressed.
- the absorbent article has a component that is located on the non-skin side of the side sheet of 1 and is directly or indirectly joined to the side sheet of 1.
- the constituent member may extend outward in the width direction from the standing edge. According to this aspect, since the rigidity of the leg gather can be increased by the constituent member, it becomes easy to maintain the flatness of the leg gather.
- the constituent member may have a liquid opaque sheet having liquid opacity.
- the liquid-impermeable sheet can prevent the excrement from seeping out to the non-skin surface side of the liquid-impermeable sheet.
- each of the pair of sheet layers may have an edge in the width direction of the side sheet of 1.
- the edge of one sheet layer of the pair of sheet layers and the edge of the other sheet layer do not overlap in the thickness direction. As a result, the edge of one sheet layer and the edge of the other sheet layer are less likely to hit the wearer's skin together, and deterioration of the touch can be suppressed.
- the number of the one or more leg elastic members may be larger than the number of the one or more three-dimensional elastic members.
- the number of the one or more leg elastic members and the number of the one or more three-dimensional elastic members may be two or more.
- the distance between the leg elastic members may be narrower than the distance between the three-dimensional elastic members.
- the absorbent article uses an adhesive to attach the pair of sheet layers to each other between the three-dimensional elastic member located closest to the non-skin surface side when the three-dimensional gather is erected and the erected edge. It may have an in-sheet joint to be joined. According to this aspect, it becomes difficult for the excrement to reach the outer sheet layer in the width direction due to the joint portion, and the leakage of the excrement generated by exuding to the outside in the width direction of the three-dimensional gather can be suppressed.
- the pair of sheet layers are not joined to each other by an adhesive in the region between the three-dimensional elastic member located closest to the non-skin surface side when the three-dimensional gather is upright and the upright edge. It may be an inner non-bonded region. According to this aspect, since a space is generated between the pair of sheet layers, it is possible to prevent excrement from continuously permeating from the inner sheet layer in the width direction to the outer sheet layer.
- the region outside the leg elastic member arranged on the outermost side in the width direction is an outer non-bonded region in which the pair of sheet layers are not bonded to each other. You can.
- the outer region in the width direction is more likely to hit the wearer's skin than the leg elastic member arranged on the outermost side in the width direction. Therefore, in the region, since the pair of sheet layers are not joined to each other, the rigidity of the region is not increased, and deterioration of the touch can be suppressed.
- the side sheet 1 in a plan view of the absorbent article, is curved outward in the width direction, at least behind the center of the absorbent article in the anteroposterior direction. However, it may have a portion extending rearward.
- the side seats are easily arranged along the shape of the wearer's body (specifically, the boundary line between the buttocks and the legs (flesh crack line)), and the wearer feels uncomfortable due to the side seats. It becomes difficult to give.
- a storage space for excrement tools
- leakage of excrement can be suppressed.
- the method for manufacturing an absorbent article includes one side sheet arranged outside the center in the width direction of the absorbent article, three-dimensional gathers, and leg gathers, and the three-dimensional object is described.
- the gather has an upright portion that can be erected by one or more three-dimensional elastic members having elasticity in the front-rear direction, and an upright edge that serves as an upright fulcrum of the upright portion, and the leg gather has the leg gather in the front-rear direction. It has a contraction region that contracts in the front-rear direction with a predetermined width by one or more leg elastic members having elasticity, and is arranged outside the width direction from the standing edge, and is arranged with the three-dimensional gather.
- the leg gather is a method for manufacturing an absorbent article for producing an absorbent article composed of a pair of sheet layers facing each other by folding back the side sheet 1 with one crease extending in the front-rear direction as a base point.
- the composite stretchable sheet having the pair of sheet layers and having elasticity has a forming step of forming a continuous sheet continuum in the front-rear direction.
- a plurality of continuous elastic members composed of a first continuous elastic member constituting the one or more three-dimensional elastic members and a second continuous elastic member constituting the one or more leg elastic members are formed on the side sheet of the above 1.
- the pair of sheet layers facing each other by folding back one side sheet is the most skin surface when the three-dimensional gather stands up. It extends continuously in the width direction from the position in contact with the three-dimensional elastic member located on the side to the position in contact with the leg elastic member arranged on the outermost side in the width direction.
- both of the pair of seat layers overlap with all the leg elastic members, it is easy to maintain the flatness of the leg gathers, and the leg gathers are easy to fit on the wearer's skin. Therefore, it is possible to manufacture an absorbent article capable of reducing the leakage of excrement while facilitating the maintenance of the flatness of the leg gather.
- it is not necessary to fold the side sheet continuum a plurality of times to form the sheet continuum it is possible to suppress an increase in the manufacturing process.
- the forming step is performed in an intermediate region between a first elastic region in which the first continuous elastic member is arranged and a second elastic region in which the second continuous elastic member is arranged. It may further have a step of applying an adhesive that joins the sidesheet continuums together.
- the intermediate region has lower rigidity than the first elastic region and the second elastic region because the continuous elastic member is not arranged. Therefore, the rigidity of the intermediate region can be increased by applying an adhesive in the intermediate region and joining the side sheet continuums to each other. As a result, wrinkles are less likely to occur in the sheet continuum when the sheet continuum is joined to another member, and the sheet continuum can be appropriately joined to the other member.
- the composite stretchable sheet has a low stretchable region at the anterior-posterior end of the composite stretchable sheet, which has a lower stretchable force than the central portion of the composite stretchable sheet in the front-rear direction.
- the step of forming the low expansion / contraction region in the sheet continuum and the sheet continuum are arranged on the non-skin surface side of the side sheet of 1 at least in a region overlapping the low expansion / contraction region. It may have a step of joining the constituent members to be joined to a continuous body. According to this aspect, this makes it difficult for the sheet continuum to shrink in the low expansion / contraction region, so that the sheet continuum can be easily joined to the continuum.
- the low expansion / contraction region in the step of forming the low expansion / contraction region, may be formed by squeezing the sheet continuum and cutting the continuous elastic member.
- a low expansion and contraction region can be formed and the rigidity of the sheet continuum can be increased by pressing.
- the sheet continuum is less likely to shrink, so that the sheet continuum can be easily joined to the continuum.
- the side sheet of 1 in a plan view of the absorbent article, is at least posterior to the center of the absorbent article in the anteroposterior direction, and is outside in the width direction.
- the step of bending the sheet continuum and the curved sheet continuum are arranged on the non-skin surface side of the side sheet of 1 so as to have a portion extending backward while being curved toward. It may have a step of joining the constituent members to a continuous body.
- the side seats are easily arranged along the shape of the wearer's body (specifically, the boundary line between the buttocks and the legs (flesh crack line)), and the wearer feels uncomfortable due to the side seats.
- the manufacturing method provides a body adhesive for joining the sheet continuum to a continuum of continuous components arranged on the non-skin surface side of the side sheet of 1. It may have a step of applying to a sheet continuum. In the step of curving the sheet continuum, the sheet continuum coated with the main body adhesive may be curved. According to this aspect, it is not necessary to apply a high degree of control for applying the main body adhesive along the curvature of the sheet continuum, and it becomes easy to apply the main body adhesive at a target position.
- the side sheet of the above 1 absorbs at least the absorption.
- the sheet may have a step of joining the sheet to a continuous body in which the constituent members arranged on the non-skin surface side of the side sheet of 1 above are joined.
- the force applied to the inside in the width direction and the force applied to the outside in the width direction are alternately and repeatedly applied to the sheet continuum, so that the sheet continuum may not be curved as intended. is there. Therefore, by individually bending the composite telescopic sheet, the composite telescopic sheet can be curved as intended.
- the absorbent article is, for example, a pants-type disposable diaper, a tape-type disposable diaper, or a shorts-type sanitary napkin.
- the absorbent article of the embodiment is a pants-type disposable diaper.
- FIG. 1 is a schematic front view of the absorbent article 1 according to the present embodiment.
- FIG. 2 is a schematic plan view of the absorbent article 1 according to the present embodiment. The schematic plan view shown in FIG. 2 shows an stretched state in which the absorbent article 1 is stretched to a state in which wrinkles are not formed in a state where the side joint portion 18 described later is unfolded.
- FIG. 3 is a schematic cross-sectional view taken along the F3-F3 cross section shown in FIG.
- FIG. 4 is a schematic cross-sectional view of the absorbent article shown in FIG.
- FIG. 4A is a schematic cross-sectional view of the absorbent article at a position from the front waist circumference region of the inseam region, and is a schematic cross-sectional view along the F4A-F4A cross section shown in FIG.
- FIG. 4B is a schematic cross-sectional view of the absorbent article at a position from the rear waist circumference region of the inseam region, and is a schematic cross-sectional view along the F4B-F4B cross section shown in FIG.
- FIG. 5 is a schematic plan view of the absorbent article 1 according to the present embodiment.
- FIG. 6 is a diagram for explaining three-dimensional gathers.
- FIG. 6 is a diagram for explaining three-dimensional gathers.
- FIG. 6 is a diagram showing a state in which three-dimensional gathers are erected in the F6-F6 cross section shown in FIG.
- the members are separated in the thickness direction, they are in contact with each other in the thickness direction in the actual product.
- the absorbent article 1 has a front-rear direction L and a width direction W that are orthogonal to each other.
- the anteroposterior direction L is defined by the direction extending to the anterior side and the posterior side of the body.
- the anteroposterior direction L is a direction extending anterior-posteriorly in the deployed absorbent article 1.
- the absorbent article 1 has an orthogonal thickness direction T in both the front-rear direction L and the width direction W.
- the thickness direction T extends to the skin surface side T1 facing the wearer side and the non-skin surface side T2 on the side opposite to the skin surface side.
- the absorbent article 1 has a front waist circumference area S1, a rear waist circumference area S2, and an inseam area S3.
- the front waist circumference area S1 is a region facing the front waist circumference (abdomen) of the wearer.
- the rear waist circumference area S2 is an area facing the rear waist circumference (back) of the wearer, and includes an area on which the body (buttocks) is placed when worn.
- the inseam area S3 is located in the inseam of the wearer and is a region sandwiched between the front waist area S1 and the rear waist area S2. As shown in FIG.
- a side joint portion 18 may be provided in which the end portion of the front waist circumference region S1 in the width direction W and the end portion of the rear waist circumference region S2 in the width direction W are joined.
- the side joint portion 18 is defined by a portion in which the outer portion of the front waist circumference region S1 and the outer portion of the rear waist circumference region S2 are locked to each other.
- the absorbent article 1 in the state where the side joint 18 is formed, the absorbent article 1 has a waist opening 16 through which the wearer's body is passed and a pair of legs into which the wearer's legs are inserted.
- the leg circumference opening 17 is formed.
- the waist opening 16 may be defined by the front end edge S1F of the front waist circumference area S1 and the rear end edge S2R of the rear waist circumference area S2.
- FIG. 2 shows a state in which the joint at the side joint portion 18 is released and the absorbent article 1 is unfolded.
- the side joint portion 18 may extend along the front-rear direction L in each of the front exterior body 20 and the rear exterior body 30.
- the boundary between the front waist area S1 and the inseam area S3 may be defined by the rear end edge of the side joint 18 provided on the front exterior body 20.
- the boundary between the rear waist circumference area S2 and the inseam area S3 may be defined by the front end edge of the side joint portion 18 provided on the rear exterior body 30.
- the inseam area S3 may be an area provided with the leg circumference opening 17.
- the outer portion in the present invention is a portion that occupies a certain range in the width direction W including the outer edge in the width direction W, and the outer edge is an outer edge in the width direction W.
- the inner portion in the present invention is a portion that occupies a certain range in the width direction W including the inner edge in the width direction W, and the inner edge is an inner edge in the width direction W.
- the front end portion and the rear end portion in the present invention are portions that occupy a certain range in the front-rear direction L including the edge in the front-rear direction L, and the front end edge and the rear end edge are edges in the front-rear direction L.
- the outer edge includes a front edge and a trailing edge, and the outer edge includes a front edge and a trailing edge.
- the absorbent article 1 may have an exterior body 15 and a main body 40.
- the exterior body 15 overlaps the main body 40 in the thickness direction T.
- the exterior body 15 may have a front exterior body 20 arranged in the front waist circumference region S1 and a rear exterior body 30 arranged in the rear waist circumference region S2.
- the front exterior body 20 is an exterior body arranged on the non-skin surface side T2 of the main body portion 40 in the front waist circumference region S1.
- the rear exterior body 30 is an exterior body that is separated from the front exterior body 20 in the front-rear direction L and is arranged on the non-skin surface side T2 of the main body portion 40 in the rear waist circumference region S2.
- the exterior body 15 may have a cover sheet arranged on the skin surface side T1 of the main body portion 40.
- the cover sheet includes a front cover sheet 27 provided on the skin surface side T1 of the main body portion 40 of the front waist circumference area S1 and a rear cover sheet 37 provided on the skin surface side T1 of the main body portion 40 of the rear waist circumference area S2.
- the front cover sheet 27 and the rear cover sheet 37 may be made of a sheet such as a non-woven fabric.
- the front cover sheet 27 may be composed of a portion in which the sheet constituting the front exterior body 20 is folded back to the skin surface side T1, or is composed of a sheet separate from the sheet constituting the front exterior body 20. May be good.
- the rear cover sheet 37 may be composed of a portion in which the sheet constituting the rear exterior body 30 is folded back to the skin surface side T1, or is separate from the sheet constituting the rear exterior body 30. It may be composed of a sheet of.
- the front exterior body 20 and the rear exterior body 30 may be made of a sheet such as a non-woven fabric.
- the front exterior body 20 may have a first front seat 25 and a second front seat 26 located on the non-skin surface side T2 of the first front seat 25.
- the front exterior body 20 may further include seats other than the first front seat 25 and the second front seat 26.
- the rear exterior body 30 may have a plurality of sheets.
- the front exterior body 20 may have a first rear seat 35 and a second rear seat 36 located on the non-skin surface side T2 of the first rear seat 35.
- the rear exterior body 30 may further include seats other than the first rear seat 35 and the second rear seat 36.
- the exterior body 15 may have a waist elastic member WE having elasticity in the width direction W.
- the front waist elastic member 22 which is the waist elastic member WE having elasticity in the width direction W may be arranged in the front waist circumference region S1.
- a rear waist elastic member 32 which is a waist elastic member WE having elasticity in the width direction W, may be arranged in the rear waist circumference region S2.
- the front waist elastic member 22 may be arranged between the first front seat 25 and the second front seat 26, and the rear waist elastic member 32 is arranged between the first rear seat 35 and the second rear seat 36. May be done.
- the waist elastic member WE may be composed of, for example, a thread rubber stretchable in the width direction W or an elastic sheet stretchable in the width direction W.
- the waist elastic member WE may be composed of, for example, the exterior body 15 itself made of a stretchable sheet.
- the waist elastic member WE of the present embodiment is made of thread rubber.
- the main body 40 is arranged at least in the inseam area S3.
- the main body portion 40 may be arranged over the front waist circumference area S1, the rear waist circumference area S2, and the inseam area S3.
- the main body 40 is configured as a separate body from the front exterior body 20 and the rear exterior body 30, and is joined to the front exterior body 20 and the rear exterior body 30 in the front waist circumference area S1 and the rear waist circumference region S2, respectively.
- the main body 40 may have an absorbent main body 41 and a pair of composite elastic sheets 60 arranged on the skin surface side T1 of the absorbent main body 41.
- the absorbent body 41 has at least an absorbent core 50.
- the absorption core 50 contains an absorption material.
- the absorption core 50 may contain, for example, ground pulp or a highly absorbent polymer (SAP), or a mixture thereof.
- SAP highly absorbent polymer
- the absorption core 50 is arranged at least in the inseam area S3.
- the absorption core 50 may be arranged in the front waist circumference region S1 and may be arranged in the rear waist circumference region S2.
- the absorption core 50 may extend from the front waist circumference region S1 to the rear waist circumference region S2 in the front-rear direction L.
- the absorption core 50 may be covered by a core wrap.
- the absorbent main body 41 includes a center sheet 43 located on the skin surface side T1 of the absorbing core 50, a liquid impermeable sheet 46 located on the non-skin surface side T2 of the absorbing core 50, and liquid impermeable. It may have a non-skin surface sheet 47 arranged on the non-skin surface side T2 of the transparent sheet 46.
- the absorbent body 41 of the present embodiment has a center sheet 43, a liquid-impermeable sheet 46, and a non-skin surface sheet 47 from the skin surface side T1 to the non-skin surface side T2 in the region in front of the absorption core 50. They are arranged in the order of.
- the center sheet 43, the absorption core 50, the liquid permeable sheet 46, and the non-skin surface sheet 47 are arranged in this order from the skin surface side T1 to the non-skin surface side T2.
- the center sheet 43 and the liquid impermeable sheet 46 may be arranged with the absorption core 50 interposed therebetween in the thickness direction T.
- the center sheet 43 may have liquid permeability, and may be made of, for example, a non-woven fabric.
- the center sheet 43 covers the center of the absorption core 50 in the width direction W.
- the liquid-impermeable sheet 46 may be liquid-impermeable, and may be made of, for example, a film. As shown in FIG. 4, the liquid-impermeable sheet 46 may be arranged on the non-skin surface side T2 rather than the side sheet 62.
- the non-skin surface sheet 47 may be made of, for example, a non-woven fabric.
- the absorbent main body 41 may have a non-skin side side sheet 48 arranged outside the absorption core 50 in the width direction W.
- the non-skin side side sheet 48 may be arranged on the non-skin side T2 rather than the side sheet 62.
- the non-skin side side sheet 48 may be made of, for example, a non-woven fabric.
- the absorbent body 41 does not have to have the non-skin side side sheet 48.
- the absorbent main body 41 is joined to the exterior body 15 via the main body joint MB.
- the absorbent main body 41 is joined to the front exterior body 20 via the front main body joint 28, and is joined to the rear exterior 30 via the rear main body joint 38.
- the absorbent article 1 may be provided with a non-bonded region NBR in which the absorbent main body 41 and the exterior body 15 are not bonded.
- the length of the absorbent body 41 in the width direction W at the position from the rear waist circumference area of the inseam area S3 is the length of the absorbent body 41 at the position from the front waist circumference area of the inseam area S3. It may be longer than the length of W in the width direction.
- the outer edge of the absorbent body 41 may extend in the front-rear direction L along the composite telescopic sheet 60.
- the pair of composite elastic sheets 60 extend in the front-rear direction L at both side portions of the absorbent main body 41 and are joined to the absorbent main body 41.
- the composite elastic sheet 60 has elasticity in the front-rear direction L.
- the composite telescopic sheet 60 has a pair of sheet layers 62p, as will be described later.
- the pair of composite elastic sheets 60 may have a pair of side sheets 62, a three-dimensional elastic member 75, and a leg elastic member 85.
- the side sheet 62 is arranged outside the center C of the width direction W of the absorbent article 1 in the width direction W.
- the side sheet 62 covers the outer portion of the center sheet 43 on the skin surface side T1 of the center sheet 43.
- the side sheet 62 is composed of one sheet.
- the single sheet constituting the side sheet may be a single sheet or a single laminated sheet in which the sheets are laminated in the thickness direction T.
- the side sheet 62 of 1 extends rearward while curving outward in the width direction W, at least behind the center Lc of the absorbent article 1 in the front-rear direction L. May have a portion that is.
- the maximum width between the pair of side seats 62 in the rear inseam area S3 is larger than the maximum width between the pair of side seats 62 in the front inseam area S3.
- the side seat 62 extends in the front-rear direction L while being curved. Therefore, in the inseam region S3 on the front side, the side seat 62 may be joined to the center seat 43 and the non-skin side side seat 48. In the rear inseam region S3, the side sheet 62 may be joined to the non-skin side side sheet 48 and the non-skin surface sheet 47.
- the side sheet 62 is folded back from the first fold FL1 which is one fold extending in the front-rear direction L from the side sheet 62 of 1.
- the side sheet 62 of 1 may be folded back so that the first fold FL1 is arranged in the three-dimensional gather 70 described later. Therefore, the first fold FL1 is arranged inside the side sheet 62 in the width direction W.
- the edge 62E of the side sheet 62 in the width direction W is arranged outside the side sheet 62 in the width direction W, that is, on the leg circumference opening 17 side.
- the edge 62E of the side sheet 62 is the edge (edge having a cut surface) of the side sheet 62 itself.
- a pair of sheet layers 62p facing each other are formed by folding back the side sheet 62 of 1 with the first fold FL1 as a base point.
- the pair of sheet layers 62p has a first sheet layer 621 and a second sheet layer 622.
- the first sheet layer 621 is arranged at least outside the width direction W in a state where the three-dimensional gathers are erected, and the second sheet layer 622 is arranged at least inside the width direction W.
- the first sheet layer 621 is arranged on the skin surface side T1 in an elongated state in which the absorbent article is extended until the wrinkles of the three-dimensional gather disappear, and the second sheet layer 622 is arranged on the non-skin surface side T2.
- the first fold FL1 may define the boundary between the first sheet layer 621 and the second sheet layer 622.
- the pair of sheet layers 62p themselves may be further folded back from the second fold FL2, which is a fold extending in the front-rear direction L, inside the width direction W of the side sheet 62. ..
- the first sheet layer 621 may be arranged on the non-skin surface side T2
- the second sheet layer 622 may be arranged on the skin surface side T1.
- Each of the pair of sheet layers 62p may have an edge 62E of one side sheet 62.
- the edge 62E of the first sheet layer 621 and the edge 62E of the second sheet layer 622 overlap in the thickness direction T.
- the edge 62E of the side sheet 62 may be arranged inside the width direction W of the absorbent body 41 with respect to the side edge in the width direction W. As a result, the edge 62E of the side sheet 62 is less likely to hit the wearer's skin, and deterioration of the touch can be suppressed.
- the three-dimensional elastic member 75 is an elastic member having elasticity in the front-rear direction L. Due to the contraction of the three-dimensional elastic member 75, the three-dimensional gather 70 can stand up on the skin surface side T1.
- the three-dimensional elastic member 75 may be made of, for example, a rubber thread or an elastic sheet.
- the three-dimensional elastic member 75 is composed of one or more elastic members. When the number of the three-dimensional elastic members 75 is two or more, the three-dimensional elastic members 75 may be arranged at intervals in the width direction W.
- the three-dimensional elastic member 75 is composed of a first three-dimensional elastic member 751 and a second three-dimensional elastic member 752. As shown in FIG.
- the first three-dimensional elastic member 751 is located on the skin surface side T1 most when the three-dimensional gather 70 stands up. Therefore, the first three-dimensional elastic member 751 is arranged at the position closest to the apex Ap of the three-dimensional gather 70.
- the second three-dimensional elastic member 752 is located on the non-skin surface side T2 most when the three-dimensional gather 70 stands up. Therefore, the second three-dimensional elastic member 752 is arranged at the position farthest from the apex Ap (first fold FL) of the three-dimensional gather 70 in the direction along the side sheet 62.
- the side sheet 62 a pair of sheet layers 62p
- the first three-dimensional elastic member 751 is the second three-dimensional elastic member. It is arranged outside the width direction W of 752. That is, the first three-dimensional elastic member 751 is arranged outside the width direction W of the second three-dimensional elastic member 752 in the non-standing state, but in the standing state, the width direction W is larger than that of the second three-dimensional elastic member 752. It may be located inside the body and on the skin surface side of the second three-dimensional elastic member 752.
- the three-dimensional elastic member located closest to the skin surface side when the three-dimensional gather 70 stands is the first three-dimensional elastic member 751 in the present embodiment, but may be the second three-dimensional elastic member 752.
- the three-dimensional elastic member located closest to the skin surface side when the three-dimensional gather 70 stands may be the three-dimensional elastic member located closest to the skin surface side in the center of the inseam region in the anteroposterior direction.
- the absorbent article 1 is formed between the second three-dimensional elastic member 752 (the elastic member located on the non-skin surface side T2 most when the three-dimensional gather 70 is upright) and the upright edge 73 described later. It may have a joint portion (joint portion in the sheet) 63 for joining a pair of sheet layers 62p to each other with an adhesive.
- the joint portion 63 in the sheet may be, for example, an HMA (hot melt adhesive).
- the leg elastic member 85 is an elastic member having elasticity in the front-rear direction L.
- the leg elastic member 85 is arranged outside the standing edge 73, which is a standing fulcrum of the standing portion 72, which will be described later, in the width direction W.
- the leg elastic member 85 may be made of, for example, a rubber thread or an elastic sheet.
- the leg elastic member 85 is composed of one or more elastic members. When the number of leg elastic members 85 is 2 or more, the leg elastic members 85 may be arranged at intervals in the width direction W. When the number of leg elastic members 85 and the number of three-dimensional elastic members 75 are two or more, the distance between the leg elastic members 85 may be narrower than the distance between the three-dimensional elastic members 75 in the width direction W. Further, the number of leg elastic members 85 may be larger than the number of three-dimensional elastic members 75.
- the leg elastic member 85 is composed of a first leg elastic member 851, a second leg elastic member 852, a third leg elastic member 853, and a fourth leg elastic member 854.
- the first leg elastic member 851 is arranged on the innermost side in the width direction W
- the fourth leg elastic member 854 is arranged on the outermost side in the width direction W.
- a contraction region 85R that contracts in the front-rear direction L with a predetermined width due to the contraction of the leg elastic member 85 is provided.
- the width of the contraction region 85R is at least from the innermost leg elastic member 85 (that is, the first leg elastic member 851) to the outermost leg elastic member 85 (that is, the fourth leg elastic member 854) in the width direction W.
- the length of the contraction region 85R may be longer than the length from the innermost leg elastic member 85 to the outermost leg elastic member 85.
- the three-dimensional elastic member 75 and the leg elastic member 85 are sandwiched between a pair of sheet layers 62p. As a result, the three-dimensional elastic member 75 and the leg elastic member 85 are in contact with the sheet layer 62p.
- the region outside the width direction W with respect to the fourth leg elastic member 854 arranged on the outermost side in the width direction W may be an outer non-bonded region in which the pair of sheet layers 62p are not bonded to each other.
- the absorbent article 1 has a three-dimensional gather 70 and a leg gather 80.
- the three-dimensional gather 70 can stand on the skin surface side T1.
- the three-dimensional gather 70 may be referred to as a leak-proof cuff.
- the three-dimensional gather 70 may have a leak-proof joint portion 71, an upright portion 72, and an upright end edge 73.
- the leak-proof joint portion 71 is a portion for joining the side sheet 62 (composite telescopic sheet 60) to the absorbent main body 41.
- the leak-proof joint 71 may be made of an adhesive.
- the leak-proof joint 71 is located outside the front-rear joint portion 711 located outside the standing edge 73 in the front-rear direction L and outside the width direction W from the standing edge 73. It may have a width joint 712 to be arranged.
- the front-rear joint portion 711 may have a front joint portion 711F arranged in the front waist circumference region S1 and a rear joint portion 711R arranged in the rear waist circumference region S2.
- the standing portion 72 can stand by one or more three-dimensional elastic members 75.
- the standing portion 72 stands up by the contraction of the three-dimensional elastic member 75.
- the standing edge 73 serves as a standing fulcrum of the standing portion 72.
- the upright edge 73 is composed of an inner edge of the front-rear joint 711 (a rear edge of the front joint 711F and a front edge of the rear joint 711R) and an inner edge of the width joint 712.
- the front-rear joint portion 711 joins a portion where the side sheet 62 is folded back from the second fold FL2 as a base point and a portion which is not folded back from the second fold FL2 as a base point.
- the leg gather 80 has a contraction region 85R.
- the contraction region 85R contracts in the front-rear direction L due to the contraction of the leg elastic member 85 arranged outside the standing edge 73 in the width direction W in the inseam region S3. Further, the leg gather 80 is arranged outside the standing edge 73 in the width direction W in the extended state.
- the three-dimensional gather 70 and the leg gather 80 are composed of a pair of sheet layers 62p.
- the pair of sheet layers 62p are arranged on the outermost side in the width direction W from the position P1 in contact with the first three-dimensional elastic member 751 located closest to the skin surface when the three-dimensional gather 70 stands up. It extends continuously to the position P2 in contact with the fourth leg elastic member 854. Therefore, both of the pair of sheet layers 62p overlap all the leg elastic members 85 in the thickness direction T.
- the pair of sheet layers 62p since the pair of sheet layers 62p are arranged on the three-dimensional gather 70 formed by the first fold FL1, the pair of sheet layers 62p exceeds the first three-dimensional elastic member 751 and the first fold FL1, that is, the apex of the three-dimensional gather 70. It extends continuously to Ap. Further, the pair of sheet layers 62p extends beyond the fourth leg elastic member 854 to the outside in the width direction W.
- the constituent members arranged on the non-skin surface side T2 of 1 side sheet 62 and directly or indirectly joined to 1 side sheet 62 are standing ends. It may extend outward in the width direction W from the edge 73.
- the constituent members may overlap one or more leg elastic members 85 in the thickness direction T, and preferably overlap all leg elastic members 85.
- the constituent member is at least one of a center sheet 43, a liquid-impermeable sheet 46, a non-skin surface sheet 47, and a non-skin side side sheet 48. Therefore, for example, the liquid-impermeable sheet 46 may extend outward in the width direction W from the standing edge 73.
- the center sheet 43 and the non-skin side side sheet 48 are directly joined to the side sheet 62.
- the liquid-impermeable sheet 46 is indirectly joined to the side sheet 62 via the non-skin side side sheet 48.
- the non-skin surface sheet 47 is directly bonded to the side sheet 62 (see FIG. 4A), and is indirectly bonded to the side sheet 62 via the liquid-impermeable sheet 46 and / or the non-skin side side sheet 48. ing.
- the fourth three-dimensional elastic member 751 located on the skin surface side T1 when the three-dimensional gather 70 is erected is arranged on the outermost side in the width direction W.
- a pair of sheet layers are continuously present between the leg elastic members 854. If there is an upright edge 73 between the three-dimensional elastic member located closest to the skin surface when the three-dimensional gather is upright and the leg elastic member arranged on the outermost side in the width direction, a pair of upright edge edges 73 is present.
- the first The sheet layer 621 can prevent exudation to the outside in the width direction W. As a result, leakage of excrement generated by exuding to the outside of the width direction W of the three-dimensional gather can be suppressed.
- both of the pair of seat layers overlap all the leg elastic members 85 in the thickness direction T, it is easy to maintain the flatness of the leg gather 80, and the leg gather 80 is on the wearer's skin. It will be easier to fit.
- the first fold FL1 of the side sheet 62 is softer than the edge 62E of the side sheet 62. Therefore, since the three-dimensional elastic member 75 and the leg elastic member 85 are sandwiched between the pair of sheet layers 62p, the first fold FL1 of the side sheet 62, which is soft to the touch, hits the wearer's skin when the three-dimensional gather 70 stands up. Therefore, it is possible to suppress the deterioration of the wearing comfort of the absorbent article 1 due to the standing of the three-dimensional gather 70.
- the leg gather 80 since the constituent members such as the center sheet 43, the liquid-impermeable sheet 46, the non-skin surface sheet 47, and the non-skin side side sheet 48 extend outward in the width direction W from the standing edge 73, the leg gather 80 The rigidity of the leg gather 80 can be increased, and the flatness of the leg gather 80 can be easily maintained.
- the liquid opaque sheet 46 extends outside the width direction W from the standing edge 73, even if the excrement moves outside the width direction W from the standing edge 73, the liquid opaque sheet 46 is opaque. The sheet 46 can prevent excrement from seeping out to the non-skin surface side of the liquid-impermeable sheet 46.
- the number of leg elastic members 85 is larger than the number of three-dimensional elastic members 75.
- the rigidity of the leg gather 80 can be increased, and the flatness of the leg gather 80 can be easily maintained.
- the distance between the leg elastic members 85 is narrower than the distance between the three-dimensional elastic members 75. As a result, by arranging a large number of leg elastic members 85 per unit area, the rigidity of the leg gather 80 can be increased, and the flatness of the leg gather 80 can be easily maintained.
- the in-sheet joint portion 63 is provided between the second three-dimensional elastic member 752 and the upright edge 73, the excrement is collected by the in-sheet joint portion 63 in the outer first sheet layer in the width direction W. It becomes difficult to reach 621 (see FIG. 6). As a result, leakage of excrement generated by exuding the excrement to the outside of the width direction W of the three-dimensional gather 70 can be suppressed.
- the region outside the width direction W of the fourth leg elastic member 854 is an outer non-joining region. Since the region easily hits the wearer's skin, the rigidity of the region is not increased and deterioration of the touch can be suppressed by not joining the pair of sheet layers 62p to each other in the region.
- the side seat 62 has a portion (curved portion) extending rearward while curving outward in the width direction W on the rear side of the center Lc in the front-rear direction L. This makes it easier for the side seat 62 to be arranged along the shape of the wearer's body (specifically, the boundary line between the buttocks and the legs (flesh crack line)), giving the wearer a sense of discomfort due to the side seat 62. It becomes difficult. In addition, since a storage space for excrement (stool) can be secured, leakage of excrement can be suppressed.
- FIGS. 7 to 9 are diagrams for explaining a method for producing the absorbent article 1.
- the direction in which the component parts in the manufacturing process are conveyed is shown as the transport direction MD
- the direction intersecting the transport direction is shown as the cross direction CD
- the direction orthogonal to the transport direction MD and the cross direction CD is shown as the transverse direction TD.
- the left figure shows the member seen from the transverse direction TD (upper side)
- the right figure shows the member seen from the transport direction MD.
- the right figure of the step S11 of FIG. 7 shows a schematic cross-sectional view along the C11-C11 cross section of the left figure.
- the right figure of the step S12 of FIG. 7 shows a schematic cross-sectional view along the C12-C12 cross section of the left figure.
- the right figure of the step S13 of FIG. 7 shows a schematic cross-sectional view along the C13-C13 cross section of the left figure.
- the right figure of the step S20 of FIG. 8 shows a schematic cross-sectional view along the C20-C20 cross section of the left figure.
- the right figure of the step S30 of FIG. 8 shows a schematic cross-sectional view along the C30-C30 cross section of the left figure.
- the right figure of the step S40 of FIG. 8 shows a schematic cross-sectional view along the C40-C40 cross section of the left figure.
- the right figure of the step S60 of FIG. 9 shows a schematic cross-sectional view along the C60-C60 cross section of the left figure.
- the right figure of the step S70 of FIG. 9 shows a schematic cross-sectional view along the C70-C70 cross section of the left figure.
- the right figure of the step S80 of FIG. 9 shows a schematic cross-sectional view along the C80-C80 cross section of the left figure.
- the configuration of the manufacturing apparatus is not shown.
- CL indicates a cutting line at which the sheet continuum 60C described later is cut.
- PFL1 indicates a virtual line indicating a crease of the side sheet continuum 62C.
- the first fold FL1 is provided by folding the side sheet continuum 62C at the position of PFL1.
- the process for manufacturing the absorbent article according to the present embodiment includes steps S10 to S80.
- Step S10 is a step in which the composite telescopic sheet 60 forms a sheet continuum 60C continuous in the front-rear direction L.
- the step S10 may include a step S11, a step S12, and a step S13.
- Step S11 is a step of applying the adhesive 63C to the conveyed side sheet continuum 62C.
- the adhesive 63C is an adhesive corresponding to the joint portion 63 in the sheet.
- the adhesive 63C joins the side sheet continuums 62C to each other.
- the adhesive 63C is applied along the transport direction MD.
- the adhesive 63C may be placed in the intermediate region MR.
- the intermediate region MR is a region between the first elastic region ER1 and the second elastic region ER2.
- the first elastic region ER1 is a region in which the first continuous elastic member 75C, which will be described later, is arranged.
- the second elastic region ER2 is a region in which the second continuous elastic member 85C, which will be described later, is arranged.
- the intermediate region MR is sandwiched between the first elastic region ER1 and the second elastic region ER2 in the transport direction MD.
- Step S12 is a step of arranging a plurality of continuous elastic member CEs on the side sheet continuous body 62C.
- the plurality of continuous elastic member CEs are composed of a first continuous elastic member 75C constituting one or more three-dimensional elastic members 75 and a second continuous elastic member 85C constituting one or more leg elastic members 85.
- the continuous elastic member CE includes a three-dimensional elastic member 75 continuous in the front-rear direction L, and a leg elastic member 85 continuous in the front-rear direction L.
- the first continuous elastic member 75C may be arranged between the position (PFL1) at which the first fold FL1 is formed and the adhesive 63C in the crossing direction CD.
- the second continuous elastic member 85C may be arranged between the adhesive 63C in the crossing direction CD and one edge 62E closer to the adhesive 63C in the crossing direction CD of the side sheet continuum 62C.
- the first continuous elastic member 75C is composed of the first continuous elastic member 751C and the first continuous elastic member 752C. Therefore, the first elastic region ER1 is a region between the first continuous elastic member 751C and the first continuous elastic member 752C.
- the second continuous elastic member 85C is composed of the second continuous elastic member 851C to the second continuous elastic member 854C. Therefore, the second elastic region ER2 is a region between the second continuous elastic member 851C and the second continuous elastic member 854C.
- An adhesive is applied to the continuous elastic member CE, and by arranging the continuous elastic member CE on the side sheet continuous body 62C, the continuous elastic member CE is fixed to the side sheet continuous body 62C.
- An adhesive for fixing the continuous elastic member CE may be applied to the side sheet continuous body 62C.
- Step S13 is a step of folding back the side sheet continuum 62C once so that all of the plurality of continuous elastic member CEs are sandwiched between the side sheet continuum 62C.
- the side sheet continuous body 62C on one side is formed into a plurality of continuous elastic members with the position PFL1 serving as the first fold FL1 as a boundary. It overlaps with the side sheet continuum 62C on the other side where the CE is arranged in the transverse direction TD.
- the distance from the position PFL1 to the other end edge 62E far from the adhesive 63C of the side sheet continuous body 62C in the crossing direction CD. Is required to be greater than or equal to the distance from position PFL1 to the second continuous elastic member 854C.
- the adhesive 63C joins a pair of sheet layers 62p (first sheet layer 621 and second sheet layer 622) formed by folding back.
- step S13 and after the illustration of the adhesive 63C is omitted.
- a sheet continuum 60C having a pair of sheet layers 62p can be formed.
- the absorbent article described in FIG. 4 of Patent Document 1 Japanese Patent Application Laid-Open No. 2018-511305
- all the first continuous elastic members 75C are replaced with the side sheet continuum 62C by the first folding.
- All the second continuous elastic members 85C can be sandwiched between the side sheet continuous bodies 62C by the second folding back. Therefore, in order to form the sheet continuum 60C, it is necessary to fold the side sheet continuum 62C at least twice.
- the number of steps for forming the sheet continuum 60C can be reduced as compared with the absorbent article of FIG. 4 of Patent Document 1.
- Step S20 is a step of forming a low expansion / contraction region LER (first low expansion / contraction region LER1).
- the low stretchable region LER is a region at the end of the composite stretchable sheet 60 in the front-rear direction L and having a lower stretchable force than the central portion of the composite stretchable sheet 60 in the front-rear direction L.
- the adhesive is applied so as to overlap the continuous elastic member CE (first continuous elastic member 75C) in the transverse direction TD.
- the adhesive is applied so as to straddle the cutting line CL.
- the adhesive is applied at intervals in the transport direction MD so that the stretch force of the central portion of the composite stretchable sheet 60 in the front-rear direction L does not decrease. Due to the rigidity of the adhesive, in the region where the adhesive is applied, the elastic force of the first continuous elastic member 75C is the first continuous in the region where the adhesive is not applied (the region before and after the adhesive transport direction MD). It becomes weaker than the elastic force of the elastic member 75C. Therefore, the region to which the adhesive is applied constitutes the first low-stretch region LER1, which is the low-stretch region LER.
- Step S30 is a step of folding back the sheet continuum 60C.
- the sheet continuum 60C is joined to each other via the adhesive applied in step S20.
- Step S40 is a step of forming a low expansion / contraction region LER (second low expansion / contraction region LER2).
- the sheet continuum 60C is squeezed in the region before and after the cutting line CL in the transport direction MD.
- the continuous elastic member CE is cut.
- the cut continuous elastic member CE contracts in the transport direction MD by contraction, and the three-dimensional elastic member 75 and the leg elastic member 85 are provided.
- the region where the three-dimensional elastic member 75 and the leg elastic member 85 do not exist due to the contraction is a region where the elastic force is reduced and constitutes the second low elastic region LER2.
- Step S50 is a step of applying the main body adhesive 71C to the sheet continuum 60C.
- the main body adhesive 71C is an adhesive for joining the sheet continuous body 60C to the absorbent main body continuous body 41C in which the constituent members arranged on the non-skin surface side T2 of 1 side sheet 62 are continuous. Further, the main body adhesive 71C is an adhesive that constitutes the leak-proof joint portion 71. The main body adhesive 71C is applied to the area where the leak-proof joint 71 is arranged.
- the main body adhesive 71C may be arranged in a region overlapping the low expansion / contraction region LER.
- Step S60 is a step of bending the sheet continuum 60C.
- the sheet continuum 60C is curved so that the side sheet 62 of 1 has a curved portion.
- one side of the sheet continuum 60C in the transport direction MD is shifted to the crossing direction CD with respect to the other side of the sheet continuum 60C to obtain a sheet.
- the continuum 60C can be curved.
- the rear side of the sheet continuum 60C when the rear side of the sheet continuum 60C is shifted to one side (for example, the right side) of the crossing direction CD, the area between the next cutting line CL and the cutting line CL is in front of the sheet continuum 60C. Since the side is shifted to one side of the crossing direction CD, the rear side of the sheet continuum 60C may be shifted to the other side (for example, the left side) of the crossing direction CD. As a result, the space in the crossing direction CD is not increased, and the enormous manufacturing apparatus can be suppressed.
- step S60 is performed after the step S40, the elastic members are not continuous in the width direction W. As a result, the force applied to the crossing direction CD by the elastic member can be reduced, and the sheet continuum 60C can be curved as intended. Since the step S60 is performed after the step S50, the sheet continuum 60C coated with the main body adhesive 71C is curved.
- Step S70 is a step of joining the curved sheet continuum 60C to the absorbent body continuum 41C.
- the sheet continuous body 60C can be joined to the absorbent main body continuous body 41C via the main body adhesive 71C.
- the curved sheet continuum 60C can be joined to the absorbent main body continuum 41C at least at a position overlapping the low expansion / contraction region LER.
- the absorbent main body continuous body 41C may have the absorbent main body 41 continuous in the front-rear direction L, or may be a continuous member directly joined to the composite telescopic sheet 60. For example, after the sheet continuous body 60C and the absorbent main body continuous body 41C that does not include the non-skin surface sheet 47 continuous in the front-rear direction L are joined, the non-skin surface sheet 47 is continuous in the front-rear direction L. May be joined. By joining the curved sheet continuum 60C to the absorbent main body continuous body 41C, the main body continuous body 40C in which the main body portion 40 is continuous can be formed.
- Step S80 is a step of cutting the main body continuum 40C.
- the main body continuum 40C is cut along the cutting line CL.
- the side end portion of the main body continuum 40C in the crossing direction CD may be cut.
- the side end portion 41CE of the absorbent body continuum 41C in the crossing direction CD may be cut along the sheet continuum 60C extending in the transport direction MD.
- the main body 40 having a width on the rear side wider than the width on the front side can be manufactured.
- the absorbent article 1 can be manufactured by joining the exterior body 15 to the main body 40.
- the manufacturing method of the embodiment it is possible to manufacture the absorbent article 1 which can reduce the leakage of excrement while facilitating the maintenance of the flatness of the leg gather 80. Further, since it is not necessary to fold the side sheet continuum 62C a plurality of times to form the sheet continuum 60C, an increase in the manufacturing process can be suppressed.
- step S11 the adhesive 63C for joining the side sheet continuums 62C to each other is applied to the intermediate region MR. Since the continuous elastic member CE is not arranged, the intermediate region MR has lower rigidity than the first elastic region ER1 and the second elastic region ER2. Therefore, the rigidity of the intermediate region MR can be increased by applying the adhesive 63C in the intermediate region MR and joining the side sheet continuums 62C to each other. As a result, when the sheet continuum 60C is joined to another member (absorbent main body continuum 41C), wrinkles are less likely to occur in the sheet continuum 60C (side sheet continuum 62C), and the sheet continuum 60C is used as a separate member. Can be joined properly.
- step S70 the sheet continuum 60C is joined to the absorbent main body continuum 41C in the region overlapping the low expansion / contraction region LER.
- the sheet continuum 60C is less likely to shrink, so that the sheet continuum 60C can be easily joined to the absorbent main body continuum 41C.
- the second low expansion / contraction region LER2 is formed by pressing the sheet continuum 60C and cutting the continuous elastic member CE.
- the continuous elastic member CE By cutting the continuous elastic member CE, the second low expansion / contraction region LER2 can be formed, and the rigidity of the sheet continuous body 60C can be increased by pressing. As a result, the sheet continuum 60C is less likely to shrink, so that the sheet continuum 60C can be easily joined to the absorbent main body continuum 41C.
- step S70 the curved sheet continuum 60C is joined to the absorbent main body continuum 41C.
- This makes it easier for the side seat 62 to be arranged along the shape of the wearer's body (specifically, the boundary line between the buttocks and the legs (flesh crack line)), giving the wearer a sense of discomfort due to the side seat 62. It is possible to manufacture the absorbent article 1 which becomes difficult.
- the continuous elastic member CE can be curved as intended.
- step S60 the sheet continuum 60C coated with the main body adhesive 71C is curved. Therefore, a high degree of control for applying the main body adhesive 71C along the curvature of the sheet continuum 60C becomes unnecessary, and the main body adhesive can be easily applied to the target position.
- FIG. 10 is a schematic cross-sectional view of the absorbent article according to the modified example.
- FIG. 10A is a schematic cross-sectional view of the absorbent article 1 according to the modified example 1
- FIG. 10B is a schematic cross-sectional view of the absorbent article 1 according to the modified example 2.
- the cross section in FIG. 10 corresponds to the F4A-F4A cross section. The same description as in the embodiment will be omitted.
- Modification example 1 will be described with reference to FIG. 10A.
- the edge 62E of the side sheet 62 is arranged on the three-dimensional gather 70.
- the edge 62E of the side sheet 62 may form the apex Ap of the three-dimensional gather 70 described later.
- the in-sheet joint portion 63 may not be provided in the region between the second three-dimensional elastic member 752 and the standing edge 73. That is, the region between the second three-dimensional elastic member 752 and the standing edge 73 may be an inner non-bonded region in which the pair of sheet layers 62p are not bonded to each other. As a result, a space is generated between the pair of sheet layers 62p, so that it is possible to prevent excrement from continuously permeating from the second sheet layer 622 to the first sheet layer 621.
- Modification example 2 will be described with reference to FIG. 10B.
- the edge 62E of the first sheet layer 621 and the edge 62E of the second sheet layer 622 do not have to overlap in the thickness direction T. Therefore, the edge 62E of the first sheet layer 621 and the edge 62E of the second sheet layer 622 may be displaced in the width direction W.
- the edge 62E of the first sheet layer 621 and the edge 62E of the second sheet layer 622 are less likely to come into contact with the wearer's skin, and deterioration of the touch can be suppressed.
- the edge 62E of the first sheet layer 621 may be arranged outside the edge 62E of the second sheet layer 622 in the width direction W, and may be located outside the edge 62E of the second sheet layer 622 in the width direction W. It may be arranged inside.
- the method for producing an absorbent article may include a step of cutting the sheet continuum 60C after the step S50.
- the sheet continuum 60C can be cut along the cutting line CL.
- a step of bending the composite telescopic sheet 60 manufactured by cutting is performed.
- the bending method is the same as in step S60.
- the sheet continuum 60C when the sheet continuum 60C is curved, since the sheet continuum 60C is continuous in the transport direction MD, the sheet continuum 60C has a force applied to the inside of the crossing direction CD and the outside of the crossing direction CD. There is a possibility that the seat continuum 60C cannot be bent as intended due to the repeated alternating forces applied to the seat continuum 60C. Therefore, by individually bending the composite telescopic sheet 60, the composite telescopic sheet 60 can be curved as intended.
- the curved composite telescopic sheet 60 is joined to the absorbent main body continuum 41C in the same manner as in step S70.
- the composite telescopic sheet 60 curved as intended can be joined to the absorbent body continuum 41C, and the side sheet 62 is the shape of the wearer's body (specifically, the boundary line between the buttocks and the legs). (Filling line)), it becomes easier to arrange.
- step S11 may be performed after step S12.
- some steps of the manufacturing method may be omitted.
- one step of the step of forming the first low stretch region LER1 and the second low stretch region LER2 may be omitted, or both steps may be omitted.
- step S20 may be omitted.
Landscapes
- Health & Medical Sciences (AREA)
- Engineering & Computer Science (AREA)
- Life Sciences & Earth Sciences (AREA)
- Vascular Medicine (AREA)
- Biomedical Technology (AREA)
- Heart & Thoracic Surgery (AREA)
- Epidemiology (AREA)
- Animal Behavior & Ethology (AREA)
- General Health & Medical Sciences (AREA)
- Public Health (AREA)
- Veterinary Medicine (AREA)
- Manufacturing & Machinery (AREA)
- Botany (AREA)
- Absorbent Articles And Supports Therefor (AREA)
Abstract
レッグギャザーの平面性を維持し易くしつつも、排泄物の漏れを低減できる吸収性物品を提供する。立体ギャザー(70)とレッグギャザー(80)とは、1のサイドシート(62)を前後方向(L)に延びる1つの折り目(FL1)を基点に折り返すことによって互いに対向する一対のシート層(62p)によって構成されている。幅方向(W)において、一対のシート層(62p)は、立体ギャザー(70)の起立時に最も肌面側(T1)に位置する第1立体弾性部材(751)と接する位置(P1)から、幅方向(W)において最も外側に配置されている第4レッグ弾性部材(854)と接する位置(P2)まで、連続的に延びている。
Description
本発明は、吸収性物品、及び吸収性物品の製造方法に関する。
特許文献1の図4には、吸収性物品の前記幅方向の中心よりも前記幅方向の外側に配置される1のサイドシートと、肌面側に起立可能である立体ギャザーと、立体ギャザーよりも幅方向の外側に配置されているレッグギャザーと、を有する吸収性物品が開示されている。サイドシートは、前後方向に延びる2つの折り目を基点に折り返されている。
レッグギャザーは、一方の折り目(幅方向において外側の折り目)を基点にサイドシートを折り返すことによって構成されている。レッグギャザーは、所定の幅で前後方向に収縮する収縮領域を有するため、レッグギャザーの平面性を維持し易い。これにより、レッグギャザーが着用者の肌に面でフィットし易くなり、着用者の脚回りを局所的に圧迫することを抑制できる。
立体ギャザーは、他方の折り目(幅方向において内側の折り目)を基点にサイドシートを折り返すことによって構成されている。立体ギャザーは、前後方向に伸縮性を有する立体弾性部材によって起立可能である起立部と、起立部の起立支点となる起立端縁と、を有する。起立部は、内側の折り目を基点に折り返された折り返し部と、内側の折り目から起立端縁まで延びる非折り返し部とによって構成されている。内側の折り目から遠い折り返し部の端部は、非折り返し部へ接合されている。
折り返し部の端部は、起立端縁まで延びていないため、起立端縁付近において、吸収性物品の表面を流れて幅方向の外側へ移動した排泄物が、非折り返し部にすぐに接触して、非折り返し部に染み込み易い。その結果、排泄物が、立体ギャザーの幅方向の外側へ染み出し易く、排泄物の漏れが発生する虞がある。折り返し部の端部から起立端縁までの領域を低減するために、折り返し部が内側の折り目から起立端縁まで延びるように、すなわち、折り返し部の長さと非折り返し部の長さとが等しくなるように、サイドシートを折り返すことが考えられる。
しかしながら、サイドシートを正確に折り返すことは難しいため、折り返し部の端部と起立端縁との間に隙間が発生することがある。従って、当該隙間を通った排泄物は、非折り返し部にすぐに接触するため、立体ギャザーから排泄物が染み出す虞が依然としてあった。
そこで、レッグギャザーの平面性を維持し易くしつつも、排泄物の漏れを低減できる吸収性物品が望まれる。
一態様に係る吸収性物品は、前後方向、前記前後方向に直交する幅方向、及び厚さ方向と、前胴回り域と、後胴回り域と、前記前胴回り域及び前記後胴回り域に挟まれている股下域と、吸収性物品の前記幅方向の中心よりも前記幅方向の外側に配置される1のサイドシートと、立体ギャザーとレッグギャザーと、を有する。前記立体ギャザーは、前記前後方向に伸縮性を有する1以上の立体弾性部材によって起立可能である起立部と、前記起立部の起立支点となる起立端縁と、を有する。前記レッグギャザーは、前記前後方向に伸縮性を有する1以上のレッグ弾性部材によって所定の幅で前記前後方向に収縮する収縮領域を有し、かつ前記起立端縁よりも前記幅方向の外側に配置されている。前記立体ギャザーと前記レッグギャザーとは、前記1のサイドシートを前記前後方向に延びる1つの折り目を基点に折り返すことによって互いに対向する一対のシート層によって構成されている。前記幅方向において、前記一対のシート層は、前記立体ギャザーの起立時に最も肌面側に位置する立体弾性部材と接する位置から、前記幅方向において最も外側に配置されているレッグ弾性部材と接する位置まで、連続的に延びている。
一態様に係る吸収性物品の製造方法は、吸収性物品の幅方向の中心よりも幅方向の外側に配置される1のサイドシートと、立体ギャザーと、レッグギャザーと、を有し、前記立体ギャザーは、前後方向に伸縮性を有する1以上の立体弾性部材によって起立可能である起立部と、前記起立部の起立支点となる起立端縁と、を有し、前記レッグギャザーは、前記前後方向に伸縮性を有する1以上のレッグ弾性部材によって所定の幅で前記前後方向に収縮する収縮領域を有し、かつ前記起立端縁よりも前記幅方向の外側に配置されており、前記立体ギャザーと前記レッグギャザーとは、前記1のサイドシートを前記前後方向に延びる1つの折り目を基点に折り返すことによって互いに対向する一対のシート層によって構成されている吸収性物品を製造する吸収性物品の製造方法である。前記製造方法は、前記一対のシート層を有しかつ伸縮性を有する複合伸縮シートが前記前後方向に連続したシート連続体を形成する形成工程を有する。前記形成工程は、前記1以上の立体弾性部材を構成する第1連続弾性部材及び前記1以上のレッグ弾性部材を構成する第2連続弾性部材からなる複数の連続弾性部材を、前記1のサイドシートが前記前後方向に連続したサイドシート連続体に配置する工程と、前記複数の連続弾性部材の全てが前記サイドシート連続体に挟まれるように、前記サイドシート連続体を1回折り返す折り工程と、を有する。
(1)実施形態の概要
本明細書及び添付図面の記載により、少なくとも以下の事項が明らかとなる。
一態様に係る吸収性物品は、前後方向、前記前後方向に直交する幅方向、及び厚さ方向と、前胴回り域と、後胴回り域と、前記前胴回り域及び前記後胴回り域に挟まれている股下域と、吸収性物品の前記幅方向の中心よりも前記幅方向の外側に配置される1のサイドシートと、立体ギャザーとレッグギャザーと、を有する。前記立体ギャザーは、前記前後方向に伸縮性を有する1以上の立体弾性部材によって起立可能である起立部と、前記起立部の起立支点となる起立端縁と、を有する。前記レッグギャザーは、前記前後方向に伸縮性を有する1以上のレッグ弾性部材によって所定の幅で前記前後方向に収縮する収縮領域を有し、かつ前記起立端縁よりも前記幅方向の外側に配置されている。前記立体ギャザーと前記レッグギャザーとは、前記1のサイドシートを前記前後方向に延びる1つの折り目を基点に折り返すことによって互いに対向する一対のシート層によって構成されている。前記幅方向において、前記一対のシート層は、前記立体ギャザーの起立時に最も肌面側に位置する立体弾性部材と接する位置から、前記幅方向において最も外側に配置されているレッグ弾性部材と接する位置まで、連続的に延びている。
立体ギャザーの起立時に最も肌面側に位置する立体弾性部材から、幅方向において最も外側に配置されているレッグ弾性部材までの間に、一対のシート層が連続して存在する。立体ギャザーの起立時に最も肌面側に位置する立体弾性部材から幅方向において最も外側に配置されているレッグ弾性部材までの間に、立体ギャザーの起立端縁が存在すると、吸収性物品の表面を流れて幅方向の外側へ移動する排泄物が、一方のシート層(起立状態で幅方向の内側のシート層、伸長状態で非肌面側のシート層)から幅方向の外側へ染み出しとしても、他方のシート層(起立状態で幅方向の外側のシート層、伸長状態で肌面側のシート層)によって幅方向の外側へ染み出すことを抑制できる。これにより、立体ギャザーの幅方向の外側へ滲み出すことで発生する排泄物の漏れを抑制できる。加えて、一対のシート層の両方が、全てのレッグ弾性部材と厚さ方向Tに重なっていることにより、レッグギャザーの平面性を維持し易く、レッグギャザーが着用者の肌に面でフィットし易くなる。
好ましい一態様によれば、前記1つの折り目が前記立体ギャザーに配置されるように、前記1のサイドシートが折り返されてよい。前記1以上の立体弾性部材と前記1以上のレッグ弾性部材とが、前記一対のシート層に挟まれてよい。サイドシートの折り目は、サイドシートの端縁(切断面を有するエッジ)と比較して、肌触りがよい。従って、立体ギャザーの起立時に、肌触りの良いサイドシートの折り目が着用者の肌に当たるため、立体ギャザーの起立に起因した着け心地の悪化を抑制できる。
好ましい一態様によれば、前記吸収性物品は、前記1のサイドシートよりも非肌面側に配置され、かつ前記1のサイドシートと直接的又は間接的に接合される構成部材を有してよい。前記構成部材は、前記起立端縁よりも前記幅方向の外側へ延びてよい。本態様によれば、構成部材により、レッグギャザーの剛性を高くすることができるため、レッグギャザーの平面性を維持し易くなる。
好ましい一態様によれば、前記構成部材は、液不透過性を有する液不透過シートを有してよい。これにより、排泄物が起立端縁よりも幅方向の外側へ移動したとしても、液不透過シートによって排泄物が、液不透過シートよりも非肌面側へ染み出すことを抑制できる。
好ましい一態様によれば、前記一対のシート層のそれぞれは、前記1のサイドシートの前記幅方向における端縁を有してよい。前記一対のシート層の一方のシート層が有する前記端縁と他方のシート層が有する前記端縁とは、前記厚さ方向に重なっていない。これにより、一方のシート層の端縁と他方のシート層の端縁とが着用者の肌に一緒に当たり難くなり、肌触りの悪化を抑制することができる。
好ましい一態様によれば、前記1以上のレッグ弾性部材の数は、前記1以上の立体弾性部材の数よりも多くてよい。これにより、レッグギャザーの剛性を高くすることができ、レッグギャザーの平面性を維持し易くなる。
好ましい一態様によれば、前記1以上のレッグ弾性部材の数及び前記1以上の立体弾性部材の数は、2以上であってよい。前記幅方向において、前記レッグ弾性部材どうしの間隔は、前記立体弾性部材どうしの間隔よりも狭くてよい。これにより、レッグギャザーの剛性を高くすることができ、レッグギャザーの平面性を維持し易くなる。
好ましい一態様によれば、前記吸収性物品は、前記立体ギャザーの起立時に最も非肌面側に位置する立体弾性部材と前記起立端縁との間において、接着剤により前記一対のシート層どうしを接合するシート内接合部を有してよい。本態様によれば、排泄物が、接合部によって幅方向の外側のシート層へ到達し難くなり、立体ギャザーの幅方向の外側へ滲み出すことで発生する排泄物の漏れを抑制できる。
好ましい一態様によれば、前記立体ギャザーの起立時に最も非肌面側に位置する立体弾性部材と前記起立端縁との間の領域は、接着剤により前記一対のシート層どうしが接合されていない内側非接合領域であってよい。本態様によれば、一対のシート層の間に空間が発生するため、排泄物が、幅方向の内側のシート層から外側のシート層へ連続的に染み込むことを抑制できる。
好ましい一態様によれば、前記幅方向において最も外側に配置されている前記レッグ弾性部材よりも前記幅方向の外側の領域は、前記一対のシート層どうしが接合されていない外側非接合領域であってよい。本態様によれば、幅方向において最も外側に配置されているレッグ弾性部材よりも幅方向の外側の領域は、着用者の肌に当たり易い。従って、当該領域では、一対のシート層どうしが接合されていないため、当該領域の剛性が高くならず、肌触りの悪化を抑制できる。
好ましい一態様によれば、前記吸収性物品の平面視において、前記1のサイドシートは、少なくとも前記吸収性物品の前記前後方向の中心よりも後側において、前記幅方向の外側へ向かうように湾曲しながら後方へ延びている部分を有してよい。本態様によれば、サイドシートが着用者の身体の形状(具体的には、臀部と脚との境界線(肉割れ線))に沿って配置され易くなり、サイドシートによる違和感を着用者に与えにくくなる。加えて、排泄物(大便)の収容空間を確保できるため、排泄物の漏れを抑制できる。
一態様に係る吸収性物品の製造方法は、吸収性物品の幅方向の中心よりも幅方向の外側に配置される1のサイドシートと、立体ギャザーと、レッグギャザーと、を有し、前記立体ギャザーは、前後方向に伸縮性を有する1以上の立体弾性部材によって起立可能である起立部と、前記起立部の起立支点となる起立端縁と、を有し、前記レッグギャザーは、前記前後方向に伸縮性を有する1以上のレッグ弾性部材によって所定の幅で前記前後方向に収縮する収縮領域を有し、かつ前記起立端縁よりも前記幅方向の外側に配置されており、前記立体ギャザーと前記レッグギャザーとは、前記1のサイドシートを前記前後方向に延びる1つの折り目を基点に折り返すことによって互いに対向する一対のシート層によって構成されている吸収性物品を製造する吸収性物品の製造方法である。前記一対のシート層を有しかつ伸縮性を有する複合伸縮シートが前記前後方向に連続したシート連続体を形成する形成工程を有する。前記形成工程は、前記1以上の立体弾性部材を構成する第1連続弾性部材及び前記1以上のレッグ弾性部材を構成する第2連続弾性部材からなる複数の連続弾性部材を、前記1のサイドシートが前記前後方向に連続したサイドシート連続体に配置する工程と、前記複数の連続弾性部材の全てが前記サイドシート連続体に挟まれるように、前記サイドシート連続体を1回折り返す折り工程と、を有する。
複数の連続弾性部材の全てがサイドシート連続体に挟まれるため、製造された吸収性物品では、1のサイドシートを折り返すことによって互いに対向する一対のシート層が、立体ギャザーの起立時に最も肌面側に位置する立体弾性部材と接する位置から、幅方向において最も外側に配置されているレッグ弾性部材と接する位置まで、幅方向に連続的に延びている。加えて、一対のシート層の両方が、全てのレッグ弾性部材と重なっているため、レッグギャザーの平面性を維持し易く、レッグギャザーが着用者の肌に面でフィットし易くなる。従って、レッグギャザーの平面性を維持し易くしつつも、排泄物の漏れを低減できる吸収性物品を製造することができる。また、サイドシート連続体を複数回折り返してシート連続体を形成する必要がないため、製造工程の増加を抑制できる。
好ましい一態様によれば、前記形成工程は、前記第1連続弾性部材が配置される第1弾性領域と前記第2連続弾性部材が配置される第2弾性領域との間の中間領域に、前記サイドシート連続体どうしを接合する接着剤を塗布する工程をさらに有してよい。本態様によれば、中間領域は、連続弾性部材が配置されていないため、第1弾性領域及び第2弾性領域よりも剛性が低い。そこで、中間領域において接着剤を塗布して、サイドシート連続体どうしを接合することにより、中間領域の剛性を高めることができる。これにより、シート連続体を別部材に接合する際にシート連続体に皺が発生し難くなり、シート連続体を別部材に適切に接合することができる。
好ましい一態様によれば、前記複合伸縮シートは、前記複合伸縮シートの前記前後方向の端部において、前記複合伸縮シートの前記前後方向の中央部よりも伸縮力が低い低伸縮領域を有してよい。前記製造方法は、前記シート連続体に、前記低伸縮領域を形成する工程と、前記シート連続体を、少なくとも前記低伸縮領域と重なる領域において、前記1のサイドシートよりも非肌面側に配置される構成部材が連続した連続体と接合する工程と、を有してよい。本態様によれば、これにより、低伸縮領域ではシート連続体が縮み難くなるため、シート連続体を連続体に接合し易くすることができる。
好ましい一態様によれば、前記低伸縮領域を形成する工程では、前記シート連続体を圧搾して前記連続弾性部材を切断することにより、前記低伸縮領域を形成してよい。本態様によれば、連続弾性部材を切断することで、低伸縮領域を形成すると共に圧搾によってシート連続体の剛性を高めることができる。これにより、シート連続体がさらに縮み難くなるため、シート連続体を連続体に接合し易くすることができる。
好ましい一態様によれば、前記製造方法は、前記吸収性物品の平面視において、前記1のサイドシートが、少なくとも前記吸収性物品の前記前後方向の中心よりも後側において、前記幅方向の外側へ向かうように湾曲しながら後方へ延びている部分を有するように、前記シート連続体を湾曲する工程と、湾曲した前記シート連続体を、前記1のサイドシートよりも非肌面側に配置される構成部材が連続した連続体と接合する工程と、を有してよい。本態様によれば、サイドシートが着用者の身体の形状(具体的には、臀部と脚との境界線(肉割れ線))に沿って配置され易くなり、サイドシートによる違和感を着用者に与えにくくなる吸収性物品を製造することができる。加えて、シート連続体を湾曲させることで、シート連続体を湾曲させた後に、連続弾性部材を湾曲させながら配置する場合と比較して、連続弾性部材の位置を調整し易い。
好ましい一態様によれば、前記製造方法は、前記1のサイドシートよりも非肌面側に配置される構成部材が連続した連続体に前記シート連続体を接合するための本体接着剤を、前記シート連続体に塗布する工程を有してよい。前記シート連続体を湾曲する工程では、前記本体接着剤が塗布された前記シート連続体を湾曲してよい。本態様によれば、シート連続体の湾曲に沿って本体接着剤を塗布するための高度な制御が必要なくなり、本体接着剤を狙い通りの位置に塗布しやすくなる。
好ましい一態様によれば、前記製造方法は、前記シート連続体を切断することによって前記複合伸縮シートを形成する工程と、前記吸収性物品の平面視において、前記1のサイドシートが、少なくとも前記吸収性物品の前記前後方向の中心よりも後側において、前記幅方向の外側へ向かうように湾曲しながら後方へ延びている部分を有するように、前記複合伸縮シートを湾曲する工程と、前記複合伸縮シートを、前記1のサイドシートよりも非肌面側に配置される構成部材が連続した連続体と接合する工程と、を有してよい。シート連続体を湾曲させた場合、シート連続体には、幅方向の内側にかかる力と、幅方向の外側にかかる力とが交互に繰り返しかかるため、シート連続体を狙い通りに湾曲できない虞がある。そこで、複合伸縮シートを個別に湾曲させることで、複合伸縮シートを狙い通りに湾曲させることができる。
(2)吸収性物品の全体概略構成
以下、図面を参照して、実施形態に係る吸収性物品について説明する。なお、以下の図面の記載において、同一又は類似の部分には、同一又は類似の符号を付している。ただし、図面は模式的なものであり、各寸法の比率等は現実のものとは異なることに留意すべきである。したがって、具体的な寸法等は、以下の説明を参酌して判断すべきである。また、図面相互間においても互いの寸法の関係や比率が異なる部分が含まれ得る。
以下、図面を参照して、実施形態に係る吸収性物品について説明する。なお、以下の図面の記載において、同一又は類似の部分には、同一又は類似の符号を付している。ただし、図面は模式的なものであり、各寸法の比率等は現実のものとは異なることに留意すべきである。したがって、具体的な寸法等は、以下の説明を参酌して判断すべきである。また、図面相互間においても互いの寸法の関係や比率が異なる部分が含まれ得る。
吸収性物品は、例えば、パンツ型の使い捨ておむつ、テープ型の使い捨ておむつ、又はショーツ型の生理用ナプキンなどである。実施形態の吸収性物品は、パンツ型の使い捨ておむつである。図1は、本実施形態に係る吸収性物品1の模式正面図である。図2は、本実施形態に係る吸収性物品1の模式平面図である。図2に示す模式平面図は、後述するサイド接合部18を展開した状態において吸収性物品1を皺が形成されない状態まで伸長させた伸長状態を示している。図3は、図2に示すF3-F3断面に沿った模式断面図である。図4は、図2に示す吸収性物品の模式断面図である。図4Aは、股下域の前胴回り域よりの位置における吸収性物品の模式断面図であり、図2に示すF4A-F4A断面に沿った模式断面図である。図4Bは、股下域の後胴回り域よりの位置における吸収性物品の模式断面図であり、図2に示すF4B-F4B断面に沿った模式断面図である。図5は、本実施形態に係る吸収性物品1の模式平面図である。図6は、立体ギャザーを説明するための図である。図6は、図5に示すF6-F6断面において立体ギャザーが起立した状態を示す図である。なお、説明の便宜上、各部材が厚さ方向において離間していたとしても、実際の製品では厚さ方向に接していることに留意すべきである。
吸収性物品1は、互いに直交する前後方向L及び幅方向Wを有する。前後方向Lは、身体前側と身体後側とに延びる方向によって規定される。言い換えると、前後方向Lは、展開された吸収性物品1において前後に延びる方向である。また、吸収性物品1は、前後方向Lと幅方向Wの両方の直交する厚さ方向Tを有する。厚さ方向Tは、着用者側に向かう肌面側T1と、肌面側と反対側の非肌面側T2と、に延びる。
吸収性物品1は、前胴回り域S1と、後胴回り域S2と、股下域S3と、を有する。前胴回り域S1は、着用者の前胴回り(腹部)に対向する領域である。後胴回り域S2は、着用者の後胴回り(背部)に対向する領域であり、装着時に身体(臀部)が載せられる領域を含む。股下域S3は、着用者の股下に位置し、前胴回り域S1と後胴回り域S2との間に挟まれた領域である。図1に示すように、幅方向Wにおける前胴回り域S1の端部と、幅方向Wにおける後胴回り域S2の端部と、を接合したサイド接合部18が設けられていてよい。サイド接合部18は、前胴回り域S1の外側部と、後胴回り域S2の外側部とを互いに係止した部分によって規定される。図1に示すように、サイド接合部18が形成された状態で、吸収性物品1には、着用者の胴が通されるウエスト開口部16と、着用者の脚がそれぞれ挿入される一対の脚回り開口部17と、が形成される。ウエスト開口部16は、前胴回り域S1の前端縁S1Fと、後胴回り域S2の後端縁S2Rとによって規定されていてよい。
ここで、図2は、サイド接合部18における接合を解除し、吸収性物品1を展開した状態を示している。サイド接合部18は、前側外装体20及び後側外装体30のそれぞれにおいて、前後方向Lに沿って延びていてよい。パンツ型の吸収性物品においては、前胴回り域S1と股下域S3との境界は、前側外装体20に設けられたサイド接合部18の後端縁によって規定されていてよい。同様に、後胴回り域S2と股下域S3との境界は、後側外装体30に設けられたサイド接合部18の前端縁によって規定されていてよい。なお、股下域S3は、脚回り開口部17が設けられた領域であってもよい。
なお、本発明における外側部とは、幅方向Wにおける外縁を含む幅方向Wに一定の範囲を占める部分であり、外側縁とは、幅方向Wにおける外縁である。本発明における内側部とは、幅方向Wにおける内縁を含む幅方向Wに一定の範囲を占める部分であり、内側縁とは、幅方向Wにおける内縁である。また、本発明における前端部及び後端部は、前後方向Lにおける縁を含む前後方向Lに一定の範囲を占める部分であり、前端縁及び後端縁は、前後方向Lにおける縁である。外端部は、前端部及び後端部を含んでおり、外端縁は、前端縁及び後端縁を含んでいる。
本実施形態では、吸収性物品1は、外装体15と、本体部40と、を有していてよい。外装体15は、本体部40と厚さ方向Tに重なっている。外装体15は、前胴回り域S1に配置された前側外装体20と、後胴回り域S2に配置された後側外装体30と、を有してよい。前側外装体20は、前胴回り域S1において本体部40よりも非肌面側T2に配置されている外装体である。後側外装体30は、前側外装体20と前後方向Lに離間し、かつ後胴回り域S2において本体部40よりも非肌面側T2に配置されている外装体である。
図3に示すように、外装体15は、本体部40の肌面側T1に配置されたカバーシートを有してよい。カバーシートは、前胴回り域S1の本体部40の肌面側T1に設けられた前側カバーシート27と、後胴回り域S2の本体部40の肌面側T1に設けられた後側カバーシート37と、を有してよい。前側カバーシート27及び後側カバーシート37は、例えば不織布のようなシートから構成されていてよい。前側カバーシート27は、前側外装体20を構成するシートが肌面側T1に折り返された部分によって構成されてもよいし、前側外装体20を構成するシートとは別体のシートによって構成されてもよい。同様に、後側カバーシート37は、後側外装体30を構成するシートが肌面側T1に折り返された部分によって構成されてもよいし、後側外装体30を構成するシートとは別体のシートによって構成されてもよい。
前側外装体20及び後側外装体30は、例えば不織布のようなシートから構成されていてよい。前側外装体20は、第1前側シート25と、第1前側シート25の非肌面側T2に位置する第2前側シート26と、を有してよい。前側外装体20は、第1前側シート25、第2前側シート26以外のシートを更に備えていてよい。また、後側外装体30は、複数のシートを有してよい。前側外装体20は、第1後側シート35と、第1後側シート35の非肌面側T2に位置する第2後側シート36と、を有してよい。後側外装体30は、第1後側シート35、第2後側シート36以外のシートを更に備えていてよい。
外装体15は、幅方向Wに伸縮性を有するウエスト弾性部材WEを有してよい。具体的には、前胴回り域S1には、幅方向Wに伸縮性を有するウエスト弾性部材WEである前ウエスト弾性部材22が配置されてよい。後胴回り域S2には、幅方向Wに伸縮性を有するウエスト弾性部材WEである後ウエスト弾性部材32が配置されてよい。前ウエスト弾性部材22は、第1前側シート25と第2前側シート26の間に配置されてよく、後ウエスト弾性部材32は、第1後側シート35と第2後側シート36の間に配置されてよい。ウエスト弾性部材WEは、例えば、幅方向Wに伸縮可能な糸ゴム、又は幅方向Wに伸縮可能な弾性シートによって構成されていてよい。ウエスト弾性部材WEは、例えば伸縮可能なシートにより構成された外装体15自体によって構成されていてもよい。本実施の形態のウエスト弾性部材WEは、糸ゴムによって構成されている。
本体部40は、少なくとも股下域S3に配置されている。本体部40は、前胴回り域S1、後胴回り域S2及び股下域S3にわたって配置されてよい。本体部40は、前側外装体20及び後側外装体30とは別体として構成され、前胴回り域S1及び後胴回り域S2において、それぞれ前側外装体20及び後側外装体30と接合されていてよい。本体部40は、吸収性本体41と、吸収性本体41よりも肌面側T1に配置される一対の複合伸縮シート60と、を有してよい。
吸収性本体41は、少なくとも吸収コア50を有する。吸収コア50は、吸収材料を含む。吸収コア50は、例えば粉砕パルプもしくは高吸収性ポリマー(SAP)、又はこれらの混合物を含んでいてよい。吸収コア50は、少なくとも股下域S3に配置されている。吸収コア50は、前胴回り域S1に配置されてよく、後胴回り域S2に配置されてよい。吸収コア50は、前後方向Lにおいて、前胴回り域S1から後胴回り域S2にわたって延びていてよい。吸収コア50は、コアラップによって覆われていてよい。
図3に示すように、吸収性本体41は、吸収コア50の肌面側T1に位置するセンターシート43と、吸収コア50の非肌面側T2に位置する液不透過シート46と、液不透過シート46よりも非肌面側T2に配置された非肌面シート47と、を有してよい。本実施の形態の吸収性本体41は、吸収コア50よりも前側の領域において、肌面側T1から非肌面側T2に向かって、センターシート43、液不透過シート46、非肌面シート47の順で配置されている。また、吸収コア50と重なった領域では、肌面側T1から非肌面側T2に向かって、センターシート43、吸収コア50、液不透過シート46、非肌面シート47の順で配置されている。センターシート43と液不透過シート46は、厚さ方向Tにおいて吸収コア50を挟んで配置されてよい。
センターシート43は、液透過性を有していればよく、例えば不織布によって構成されていてよい。センターシート43は、吸収コア50の幅方向Wの中央を覆う。液不透過シート46は、液不透過性を有していればよく、例えば、フィルムによって構成されてよい。図4に示すように、液不透過シート46は、サイドシート62よりも非肌面側T2に配置されてよい。非肌面シート47は、例えば不織布によって構成されていてよい。
図4に示すように、吸収性本体41は、吸収コア50よりも幅方向Wの外側に配置される非肌側サイドシート48を有してよい。非肌側サイドシート48は、サイドシート62よりも非肌面側T2に配置されてよい。非肌側サイドシート48は、例えば不織布によって構成されてよい。なお、吸収性本体41は、非肌側サイドシート48を有さなくてもよい。
図3に示すように、吸収性本体41は、本体接合部MBを介して外装体15と接合されている。実施形態では、吸収性本体41は、前本体接合部28を介して前側外装体20と接合されており、後本体接合部38を介して後側外装体30と接合されている。一方で、図3及び図5に示すように、吸収性物品1には、吸収性本体41と外装体15とが接合されていない非接合領域NBRが設けられてよい。図2及び図4に示すように、股下域S3の後胴回り域よりの位置における吸収性本体41の幅方向Wの長さは、股下域S3の前胴回り域よりも位置における吸収性本体41の幅方向Wの長さよりも長くてよい。吸収性本体41の外側縁は、複合伸縮シート60に沿って前後方向Lに延びてよい。
一対の複合伸縮シート60は、吸収性本体41の両側部において前後方向Lに延びており、吸収性本体41と接合されている。複合伸縮シート60は、前後方向Lに伸縮性を有する。複合伸縮シート60は、後述するように、一対のシート層62pを有する。一対の複合伸縮シート60は、一対のサイドシート62、立体弾性部材75、レッグ弾性部材85を有してよい。
サイドシート62は、吸収性物品1の幅方向Wの中心Cよりも幅方向Wの外側に配置されている。サイドシート62は、センターシート43よりも肌面側T1においてセンターシート43の外側部を覆っている。サイドシート62は、1枚のシートにより構成されている。サイドシートを構成する1枚のシートは、単一のシートであってよいし、厚さ方向Tにシートが積層された1枚の積層シートであってよい。
吸収性物品1の平面視において、1のサイドシート62は、少なくとも吸収性物品1の前後方向Lの中心Lcよりも後側において、幅方向Wの外側へ向かうように湾曲しながら後方へ延びている部分を有してよい。後側の股下域S3における一対のサイドシート62間の最大幅は、前側の股下域S3における一対のサイドシート62間の最大幅よりも大きい。サイドシート62は、湾曲しながら前後方向Lに延びている。従って、前側の股下域S3では、サイドシート62は、センターシート43と非肌側サイドシート48とに接合されてよい。後側の股下域S3では、サイドシート62は、非肌側サイドシート48と非肌面シート47と接合されてよい。
サイドシート62は、1のサイドシート62を前後方向Lに延びる1つの折り目である第1折り目FL1を基点に折り返されている。サイドシート62は、第1折り目FL1が後述する立体ギャザー70に配置されるように、1のサイドシート62が折り返されてよい。従って、第1折り目FL1は、サイドシート62の幅方向Wの内側に配置されている。一方で、サイドシート62の幅方向Wにおける端縁62Eは、サイドシート62の幅方向Wの外側、すなわち、脚回り開口部17側に配置されている。サイドシート62の端縁62Eは、サイドシート62自体の端縁(切断面を有するエッジ)である。
1のサイドシート62を、第1折り目FL1を基点に折り返すことによって互いに対向する一対のシート層62pが形成されている。一対のシート層62pは、第1シート層621と第2シート層622とを有する。第1シート層621は、立体ギャザーが起立した状態において、少なくとも幅方向Wの外側に配置されており、第2シート層622は、少なくとも幅方向Wの内側に配置されている。第1シート層621は、立体ギャザーの皺が見えなくなるまで吸収性物品を伸長させた伸長状態において、肌面側T1に配置されており、第2シート層622は、非肌面側T2に配置されている。第1折り目FL1は、第1シート層621と第2シート層622との境界を規定してよい。
なお、図4に示されるように、サイドシート62の幅方向Wの内側において、前後方向Lに延びる折り目である第2折り目FL2を基点に一対のシート層62p自体がさらに折り返されていてもよい。一対のシート層62pの折り返されている部分では、第1シート層621が非肌面側T2に配置され、第2シート層622が肌面側T1に配置されてよい。
一対のシート層62pのそれぞれ、すなわち、第1シート層621と第2シート層622とは、1のサイドシート62の端縁62Eを有してよい。実施形態では、第1シート層621が有する端縁62Eと第2シート層622が有する端縁62Eとが厚さ方向Tに重なっている。図4に示すように、サイドシート62の端縁62Eは、吸収性本体41の幅方向Wにおける側端縁よりも、幅方向Wの内側に配置されてよい。これにより、サイドシート62の端縁62Eが着用者の肌に当たり難くなり、肌触りの悪化を抑制することができる。
立体弾性部材75は、前後方向Lに伸縮性を有する弾性部材である。立体弾性部材75の収縮によって、立体ギャザー70が肌面側T1に起立可能である。立体弾性部材75は、例えば、糸ゴム又は弾性シートによって構成されていてよい。立体弾性部材75は、1以上の弾性部材によって構成される。立体弾性部材75の数が2以上である場合、立体弾性部材75は、幅方向Wに間隔を空けて配置されてよい。本実施形態では、立体弾性部材75は、第1立体弾性部材751と第2立体弾性部材752によって構成されている。図6に示すように、第1立体弾性部材751は、立体ギャザー70の起立時に最も肌面側T1に位置する。従って、第1立体弾性部材751は、立体ギャザー70の頂点Apに最も近い位置に配置されている。一方、第2立体弾性部材752は、立体ギャザー70の起立時に最も非肌面側T2に位置する。従って、第2立体弾性部材752は、サイドシート62に沿った方向において立体ギャザー70の頂点Ap(第1折り目FL)から最も遠い位置に配置されている。なお、本実施形態では、サイドシート62(一対のシート層62p)は、第2折り目FL2を基点にさらに折り返されているため、図4では、第1立体弾性部材751は、第2立体弾性部材752よりも幅方向Wの外側に配置されている。すなわち、第1立体弾性部材751は、非起立状態では、第2立体弾性部材752よりも幅方向Wの外側に配置されているが、起立状態では、第2立体弾性部材752よりも幅方向Wの内側に位置し、かつ第2立体弾性部材752よりも肌面側に位置してよい。なお、立体ギャザー70の起立時に最も肌面側に位置する立体弾性部材は、本実施の形態において第1立体弾性部材751であるが、第2立体弾性部材752であってもよい。立体ギャザー70の起立時に最も肌面側に位置する立体弾性部材は、股下域の前後方向の中央において最も肌面側に位置する立体弾性部材であってよい。
図4に示すように、吸収性物品1は、第2立体弾性部材752(立体ギャザー70の起立時に最も非肌面側T2に位置する弾性部材)と後述する起立端縁73との間において、接着剤により一対のシート層62pどうしを接合する接合部(シート内接合部)63を有してよい。シート内接合部63は、例えば、HMA(ホットメルト接着剤)であってよい。
レッグ弾性部材85は、前後方向Lに伸縮性を有する弾性部材である。レッグ弾性部材85は、後述する起立部72の起立支点である起立端縁73よりも幅方向Wの外側に配置されている。レッグ弾性部材85は、例えば、糸ゴム又は弾性シートによって構成されていてよい。レッグ弾性部材85は、1以上の弾性部材によって構成される。レッグ弾性部材85の数が2以上である場合、レッグ弾性部材85は、幅方向Wに間隔を空けて配置されてよい。また、レッグ弾性部材85の数及び立体弾性部材75の数が2以上である場合、幅方向Wにおいて、レッグ弾性部材85どうしの間隔は、立体弾性部材75どうしの間隔よりも狭くてよい。また、レッグ弾性部材85の数は、立体弾性部材75の数よりも多くてよい。
本実施形態では、レッグ弾性部材85は、第1レッグ弾性部材851、第2レッグ弾性部材852、第3レッグ弾性部材853、第4レッグ弾性部材854によって構成されている。1以上のレッグ弾性部材85のうち、第1レッグ弾性部材851は、幅方向Wにおいて最も内側に配置されており、第4レッグ弾性部材854は、幅方向Wにおいて最も外側に配置されている。レッグ弾性部材85の収縮によって所定の幅で前後方向Lに収縮する収縮領域85Rが設けられる。収縮領域85Rの幅は、幅方向Wにおいて、少なくとも、最も内側のレッグ弾性部材85(すなわち、第1レッグ弾性部材851)から最も外側のレッグ弾性部材85(すなわち、第4レッグ弾性部材854)までの長さである。図4に示すように、収縮領域85Rの長さは、最も内側のレッグ弾性部材85から最も外側のレッグ弾性部材85までの長さよりも長くてよい。本実施形態では、立体弾性部材75とレッグ弾性部材85とは、一対のシート層62pに挟まれている。これにより、立体弾性部材75とレッグ弾性部材85とは、シート層62pに接している。幅方向Wにおいて最も外側に配置されている第4レッグ弾性部材854よりも幅方向Wの外側の領域は、一対のシート層62pどうしが接合されていない外側非接合領域であってよい。
吸収性物品1は、立体ギャザー70とレッグギャザー80とを有する。立体ギャザー70は、肌面側T1に起立可能である。立体ギャザー70は、防漏カフと称されてもよい。立体ギャザー70は、防漏接合部71と、起立部72と、起立端縁73と、を有してよい。防漏接合部71は、は、サイドシート62(複合伸縮シート60)を吸収性本体41と接合する部分である。防漏接合部71は、接着剤により構成されてよい。
図4及び図5に示すように、防漏接合部71は、起立端縁73よりも前後方向Lの外側に配置される前後接合部711と、起立端縁73よりも幅方向Wの外側に配置される幅接合部712と、を有してよい。前後接合部711は、前胴回り域S1に配置される前接合部711Fと、後胴回り域S2に配置される後接合部711Rと、を有してよい。起立部72は、1以上の立体弾性部材75によって起立可能である。起立部72は、立体弾性部材75の収縮によって起立する。起立端縁73は、起立部72の起立支点となる。起立端縁73は、前後接合部711の内端縁(前接合部711Fの後端縁及び後接合部711Rの前端縁)及び幅接合部712の内側縁により構成される。前後接合部711は、サイドシート62が第2折り目FL2を基点に折り返された部分と、第2折り目FL2を基点に折り返されていない部分と、を接合する。
レッグギャザー80は、収縮領域85Rを有している。収縮領域85Rは、股下域S3において、起立端縁73よりも幅方向Wの外側に配置されているレッグ弾性部材85の収縮によって前後方向Lに収縮する。また、レッグギャザー80は、伸長状態において、起立端縁73よりも幅方向Wの外側に配置されている。
立体ギャザー70とレッグギャザー80とは、一対のシート層62pによって構成されている。図6に示すように、一対のシート層62pは、立体ギャザー70の起立時に最も肌面側に位置する第1立体弾性部材751と接する位置P1から、幅方向Wにおいて最も外側に配置されている第4レッグ弾性部材854と接する位置P2まで、連続的に延びている。従って、一対のシート層62pの両方が、全てのレッグ弾性部材85と厚さ方向Tに重なっている。
本実施形態では、第1折り目FL1がする立体ギャザー70に配置されているため、一対のシート層62pは、第1立体弾性部材751を超えて、第1折り目FL1、すなわち、立体ギャザー70の頂点Apまで連続的に延びている。また、一対のシート層62pは、第4レッグ弾性部材854を超えて幅方向Wの外側まで延びている。
また、図4及び図6に示すように、1のサイドシート62よりも非肌面側T2に配置され、かつ1のサイドシート62と直接的又は間接的に接合される構成部材は、起立端縁73よりも幅方向Wの外側へ延びてよい。構成部材は、厚さ方向Tにおいて、1以上のレッグ弾性部材85と重なってよく、全てのレッグ弾性部材85と重なっていることが好ましい。
なお、本実施形態では、構成部材は、センターシート43、液不透過シート46、非肌面シート47、非肌側サイドシート48の少なくともいずれかである。従って、例えば、液不透過シート46は、起立端縁73よりも幅方向Wの外側へ延びてよい。図4A及び図4Bに示すように、センターシート43及び非肌側サイドシート48は、サイドシート62と直接的に接合されている。液不透過シート46は、非肌側サイドシート48を介してサイドシート62と間接的に接合されている。非肌面シート47は、サイドシート62と直接的に接合されており(図4A参照)、液不透過シート46及び/又は非肌側サイドシート48を介してサイドシート62と間接的に接合されている。
上述したように、本実施形態の吸収性物品1では、立体ギャザー70の起立時に最も肌面側T1に位置する第1立体弾性部材751から、幅方向Wにおいて最も外側に配置されている第4レッグ弾性部材854までの間に、一対のシート層が連続して存在する。立体ギャザーの起立時に最も肌面側に位置する立体弾性部材から幅方向において最も外側に配置されているレッグ弾性部材までの間に、起立端縁73が存在すると、起立端縁73付近において一対のシート層62pが存在する。従って、図6に示すように、吸収性物品1の表面を流れて幅方向Wの外側へ移動する排泄物Eが、第2シート層622から幅方向Wの外側へ染み出しとしても、第1シート層621によって幅方向Wの外側へ染み出すことを抑制できる。これにより、立体ギャザーの幅方向Wの外側へ滲み出すことで発生する排泄物の漏れを抑制できる。
加えて、一対のシート層の両方が、全てのレッグ弾性部材85と厚さ方向Tに重なっているため、レッグギャザー80の平面性を維持し易く、レッグギャザー80が着用者の肌に面でフィットし易くなる。また、サイドシート62の第1折り目FL1は、サイドシート62の端縁62Eと比較して、肌触りがよい。従って、立体弾性部材75とレッグ弾性部材85とが、一対のシート層62pに挟まれているため、立体ギャザー70の起立時に、肌触りの良いサイドシート62の第1折り目FL1が着用者の肌に当たるため、立体ギャザー70の起立に起因した吸収性物品1の着け心地の悪化を抑制できる。
また、センターシート43、液不透過シート46、非肌面シート47、非肌側サイドシート48などの構成部材が、起立端縁73よりも幅方向Wの外側へ延びているため、レッグギャザー80の剛性を高くすることができ、レッグギャザー80の平面性を維持し易くできる。特に、液不透過シート46が、起立端縁73よりも幅方向Wの外側へ延びていることにより、排泄物が起立端縁73よりも幅方向Wの外側へ移動したとしても、液不透過シート46によって排泄物が、液不透過シート46よりも非肌面側へ染み出すことを抑制できる。
また、レッグ弾性部材85の数は、立体弾性部材75の数よりも多い。レッグ弾性部材85を多く配置することで、レッグギャザー80の剛性を高くすることができ、レッグギャザー80の平面性を維持し易くなる。また、レッグ弾性部材85どうしの間隔は、立体弾性部材75どうしの間隔よりも狭い。これにより、単位面積当たりに、レッグ弾性部材85を多く配置することで、レッグギャザー80の剛性を高くすることができ、レッグギャザー80の平面性を維持し易くなる。
また、第2立体弾性部材752と起立端縁73との間において、シート内接合部63が設けられているため、排泄物が、シート内接合部63によって幅方向Wの外側の第1シート層621へ到達し難くなる(図6参照)。これにより、排泄物が、立体ギャザー70の幅方向Wの外側へ染み出すことで発生する排泄物の漏れを抑制できる。また、第4レッグ弾性部材854よりも幅方向Wの外側の領域は、外側非接合領域である。当該領域は、着用者の肌に当たり易いため、当該領域において一対のシート層62pどうしを接合しないことで、当該領域の剛性が高くならず、肌触りの悪化を抑制できる。
また、サイドシート62は、前後方向Lの中心Lcよりも後側において、幅方向Wの外側へ湾曲しながら後方へ延びている部分(湾曲部分)を有している。これにより、サイドシート62が着用者の身体の形状(具体的には、臀部と脚との境界線(肉割れ線))に沿って配置され易くなり、サイドシート62による違和感を着用者に与え難くなる。加えて、排泄物(大便)の収容空間を確保できるため、排泄物の漏れを抑制できる。
(3)吸収性物品の製造方法
次に、吸収性物品1の製造方法を、図7から図9を用いて説明する。図7から図9は、吸収性物品1の製造方法を説明するための図である。製造過程における構成部品を搬送する方向を搬送方向MDとして示し、当該搬送方向と交差する方向を交差方向CDとして示し、搬送方向MD及び交差方向CDに直交する方向を横断方向TDとして示す。図7から図9において、左図は、横断方向TD(上側)から見た部材を示し、右図は、搬送方向MDから見た部材を示している。具体的には、図7の工程S11の右図は、左図のC11-C11断面に沿った模式断面図を示す。図7の工程S12の右図は、左図のC12-C12断面に沿った模式断面図を示す。図7の工程S13の右図は、左図のC13-C13断面に沿った模式断面図を示す。図8の工程S20の右図は、左図のC20-C20断面に沿った模式断面図を示す。図8の工程S30の右図は、左図のC30-C30断面に沿った模式断面図を示す。図8の工程S40の右図は、左図のC40-C40断面に沿った模式断面図を示す。図8の工程S50の右図は、左図のC50-C50断面に沿った模式断面図を示す。図9の工程S60の右図は、左図のC60-C60断面に沿った模式断面図を示す。図9の工程S70の右図は、左図のC70-C70断面に沿った模式断面図を示す。図9の工程S80の右図は、左図のC80-C80断面に沿った模式断面図を示す。なお、説明の便宜上、製造装置の構成は、図示していない。
次に、吸収性物品1の製造方法を、図7から図9を用いて説明する。図7から図9は、吸収性物品1の製造方法を説明するための図である。製造過程における構成部品を搬送する方向を搬送方向MDとして示し、当該搬送方向と交差する方向を交差方向CDとして示し、搬送方向MD及び交差方向CDに直交する方向を横断方向TDとして示す。図7から図9において、左図は、横断方向TD(上側)から見た部材を示し、右図は、搬送方向MDから見た部材を示している。具体的には、図7の工程S11の右図は、左図のC11-C11断面に沿った模式断面図を示す。図7の工程S12の右図は、左図のC12-C12断面に沿った模式断面図を示す。図7の工程S13の右図は、左図のC13-C13断面に沿った模式断面図を示す。図8の工程S20の右図は、左図のC20-C20断面に沿った模式断面図を示す。図8の工程S30の右図は、左図のC30-C30断面に沿った模式断面図を示す。図8の工程S40の右図は、左図のC40-C40断面に沿った模式断面図を示す。図8の工程S50の右図は、左図のC50-C50断面に沿った模式断面図を示す。図9の工程S60の右図は、左図のC60-C60断面に沿った模式断面図を示す。図9の工程S70の右図は、左図のC70-C70断面に沿った模式断面図を示す。図9の工程S80の右図は、左図のC80-C80断面に沿った模式断面図を示す。なお、説明の便宜上、製造装置の構成は、図示していない。
なお、CLは、後述するシート連続体60Cが切断される切断線を示す。PFL1は、サイドシート連続体62Cの折り目を示す仮想線を示す。サイドシート連続体62CがPFL1の位置で折られることにより、第1折り目FL1が設けられる。以下において、説明の便宜のために、吸収性物品1の幅方向Wの一方側の製造を主に説明するが、吸収性物品1の幅方向Wの他方側も同様に製造されることは勿論である。図7から図9に示すように、本実施形態に係る吸収性物品の製造工程は、工程S10から工程S80を有する。
工程S10は、複合伸縮シート60が前後方向Lに連続したシート連続体60Cを形成する工程である。工程S10は、工程S11と、工程S12と、工程S13と、を有してよい。工程S11は、搬送されているサイドシート連続体62Cに接着剤63Cを塗布する工程である。サイドシート連続体62Cは、1のサイドシート62が前後方向Lに連続したものである。接着剤63Cは、シート内接合部63に対応する接着剤である。接着剤63Cは、サイドシート連続体62Cどうしを接合するものである。接着剤63Cは、搬送方向MDに沿って塗布されている。接着剤63Cは、中間領域MRに配置してよい。中間領域MRは、第1弾性領域ER1と第2弾性領域ER2との間の領域である。第1弾性領域ER1は、後述する第1連続弾性部材75Cが配置される領域である。第2弾性領域ER2は、後述する第2連続弾性部材85Cが配置される領域である。中間領域MRは、搬送方向MDにおいて、第1弾性領域ER1と第2弾性領域ER2とに挟まれている。
工程S12は、複数の連続弾性部材CEをサイドシート連続体62Cに配置する工程である。複数の連続弾性部材CEは、1以上の立体弾性部材75を構成する第1連続弾性部材75Cと1以上のレッグ弾性部材85を構成する第2連続弾性部材85Cとからなる。連続弾性部材CEは、立体弾性部材75が前後方向Lに連続したものを含んでおり、レッグ弾性部材85が前後方向Lに連続したものを含んでいる。第1連続弾性部材75Cは、交差方向CDにおいて、第1折り目FL1となる位置(PFL1)と接着剤63Cとの間に配置されてよい。第2連続弾性部材85Cは、交差方向CDにおいて、接着剤63Cと、サイドシート連続体62Cの交差方向CDにおいて接着剤63Cに近い一方の端縁62Eとの間に配置されてよい。
実施形態では、第1連続弾性部材75Cは、第1連続弾性部材751Cと第1連続弾性部材752Cとにより構成される。従って、第1弾性領域ER1は、第1連続弾性部材751Cから第1連続弾性部材752Cまでの間の領域である。同様に、第2連続弾性部材85Cは、第2連続弾性部材851Cから第2連続弾性部材854Cにより構成される。従って、第2弾性領域ER2は、第2連続弾性部材851Cから第2連続弾性部材854Cまでの間の領域である。連続弾性部材CEには、接着剤が塗布されており、連続弾性部材CEをサイドシート連続体62Cに配置することにより、連続弾性部材CEがサイドシート連続体62Cに固定される。なお、サイドシート連続体62Cに連続弾性部材CEを固定するための接着剤を塗布してもよい。
工程S13は、複数の連続弾性部材CEの全てがサイドシート連続体62Cに挟まれるように、サイドシート連続体62Cを1回折り返す工程である。第1折り目FL1となる位置PFL1を境界として、複数の連続弾性部材CEが配置されていない一方側のサイドシート連続体62Cを折り返すことによって、一方側のサイドシート連続体62Cを複数の連続弾性部材CEが配置されている他方側のサイドシート連続体62Cと、横断方向TDに重ねる。なお、複数の連続弾性部材CEの全てをサイドシート連続体62Cに挟むためには、交差方向CDにおいて、位置PFL1から、サイドシート連続体62Cの接着剤63Cに遠い他方の端縁62Eまでの距離が、位置PFL1から第2連続弾性部材854Cまでの距離以上であることが必要である。接着剤63Cは、折り返しによって形成された一対のシート層62p(第1シート層621と第2シート層622)を接合する。なお、工程S13以降では、接着剤63Cの図示が省略されている。
以上の工程により、一対のシート層62pを有するシート連続体60Cを形成することができる。なお、特許文献1(特表2018-511385号公報)の図4に記載の吸収性物品を製造しようとした場合、1回目の折り返しによって、全ての第1連続弾性部材75Cをサイドシート連続体62Cに挟んで、2回目の折り返しによって、全ての第2連続弾性部材85Cをサイドシート連続体62Cに挟むことができる。従って、シート連続体60Cを形成するために、サイドシート連続体62Cを少なくとも2回以上折り返す必要がある。特許文献1の図4の吸収性物品と比較して、シート連続体60Cを形成する工程数を少なくすることができる。
工程S20は、低伸縮領域LER(第1低伸縮領域LER1)を形成する工程である。低伸縮領域LERは、複合伸縮シート60の前後方向Lの端部において、複合伸縮シート60の前後方向Lの中央部よりも伸縮力が低い領域である。
図8に示すように、接着剤が横断方向TDにおいて連続弾性部材CE(第1連続弾性部材75C)と重なるように塗布する。接着剤は、切断線CLに跨がるように塗布されている。一方で、複合伸縮シート60の前後方向Lの中央部の伸縮力が低下しないように、搬送方向MDにおいて間隔を空けて接着剤が塗布されている。接着剤の剛性によって、接着剤が塗布された領域では、第1連続弾性部材75Cの弾性力が、接着剤が塗布されていない領域(接着剤の搬送方向MDの前後の領域)における第1連続弾性部材75Cの弾性力と比較して弱くなる。従って、接着剤が塗布された領域は、低伸縮領域LERである第1低伸縮領域LER1を構成する。
工程S30は、シート連続体60Cを折り返す工程である。第1折り目FL1側のシート連続体60Cを折り返す事によって、工程S20で塗布された接着剤を介してシート連続体60Cどうしを接合する。
工程S40は、低伸縮領域LER(第2低伸縮領域LER2)を形成する工程である。具体的には、搬送方向MDにおいて切断線CLの前後の領域において、シート連続体60Cを圧搾する。これにより、連続弾性部材CEが切断される。切断された連続弾性部材CEは収縮によって搬送方向MDに収縮し、立体弾性部材75及びレッグ弾性部材85が設けられる。収縮によって立体弾性部材75及びレッグ弾性部材85が存在しなくなった領域は、伸縮力が低下した領域であり第2低伸縮領域LER2を構成する。
工程S50は、本体接着剤71Cをシート連続体60Cに塗布する工程である。本体接着剤71Cは、1のサイドシート62よりも非肌面側T2に配置される構成部材が連続した吸収性本体連続体41Cにシート連続体60Cを接合するための接着剤である。また、本体接着剤71Cは、防漏接合部71を構成する接着剤である。防漏接合部71が配置される領域に本体接着剤71Cを塗布する。本体接着剤71Cは、低伸縮領域LERと重なる領域に配置されてよい。
工程S60は、シート連続体60Cを湾曲する工程である。吸収性物品1の平面視において、1のサイドシート62が湾曲部分を有するように、シート連続体60Cを湾曲する。搬送方向MDにおける切断線CLと切断線CLとの間の領域で、搬送方向MDにおけるシート連続体60Cの一方側をシート連続体60Cの他方側に対して交差方向CDにズラすことで、シート連続体60Cを湾曲させることができる。
なお、例えば、シート連続体60Cの後側を交差方向CDの一方側(例えば、右側)にズラした場合、次の切断線CLと切断線CLとの間の領域では、シート連続体60Cの前側が交差方向CDの一方側にズレているため、シート連続体60Cの後側を交差方向CDの他方側(例えば、左側)へズラしてよい。これにより、交差方向CDにおけるスペースが大きくならず、製造装置の巨大化を抑えることができる。
工程S60は、工程S40の後に行われるため、弾性部材が幅方向Wに連続していない。これにより、弾性部材によって交差方向CDにかかる力を低減することができ、シート連続体60Cを狙い通りに湾曲させることができる。なお、工程S60は、工程S50の後に行われるため、本体接着剤71Cが塗布されたシート連続体60Cを湾曲している。
工程S70では、湾曲したシート連続体60Cを吸収性本体連続体41Cと接合する工程である。シート連続体60Cを吸収性本体連続体41C上に配置することで、シート連続体60Cを本体接着剤71Cを介して吸収性本体連続体41Cと接合できる。
本体接着剤71Cは、低伸縮領域LERと重なる領域に配置されている場合、少なくとも低伸縮領域LERと重なる位置で、湾曲したシート連続体60Cを吸収性本体連続体41Cと接合できる。
なお、吸収性本体連続体41Cは、吸収性本体41が前後方向Lに連続したものであってもよいし、複合伸縮シート60と直接接合される部材が連続したものであってもよい。例えば、シート連続体60Cと、非肌面シート47が前後方向Lに連続したものを含まない吸収性本体連続体41Cとが接合された後に、非肌面シート47が前後方向Lに連続したものが接合されてよい。湾曲したシート連続体60Cを吸収性本体連続体41Cと接合することで、本体部40が連続した本体連続体40Cを形成することができる。
工程S80では、本体連続体40Cを切断する工程である。本体連続体40Cを切断線CLに沿って切断する。また、交差方向CDにおける本体連続体40Cの側端部を切断してよい。具体的には、交差方向CDにおける吸収性本体連続体41Cの側端部41CEを、搬送方向MDに延びるシート連続体60Cに沿って、切断してよい。これにより、後側の幅が、前側の幅よりも広い本体部40を製造することができる。以後、本体部40に外装体15を接合することで、吸収性物品1を製造することができる。
以上のように、実施形態の製造方法によれば、レッグギャザー80の平面性を維持し易くしつつも、排泄物の漏れを低減できる吸収性物品1を製造することができる。また、サイドシート連続体62Cを複数回折り返して、シート連続体60Cを形成する必要がないため、製造工程の増加を抑制できる。
また、工程S11では、中間領域MRに、サイドシート連続体62Cどうしを接合する接着剤63Cを塗布する。中間領域MRは、連続弾性部材CEが配置されていないため、第1弾性領域ER1及び第2弾性領域ER2よりも剛性が低い。そこで、中間領域MRにおいて接着剤63Cを塗布して、サイドシート連続体62Cどうしを接合することにより、中間領域MRの剛性を高めることができる。これにより、シート連続体60Cを別部材(吸収性本体連続体41C)に接合する際にシート連続体60C(サイドシート連続体62C)に皺が発生し難くなり、シート連続体60Cを別部材に適切に接合することができる。
また、工程S70では、低伸縮領域LERと重なる領域において、シート連続体60Cを吸収性本体連続体41Cと接合している。これにより、低伸縮領域LERでは、シート連続体60Cが縮み難くなるため、シート連続体60Cを吸収性本体連続体41Cに接合し易くすることができる。
また、工程S40では、シート連続体60Cを圧搾して連続弾性部材CEを切断することにより、第2低伸縮領域LER2を形成している。連続弾性部材CEを切断することで、第2低伸縮領域LER2を形成すると共に圧搾によってシート連続体60Cの剛性を高めることができる。これにより、シート連続体60Cがさらに縮み難くなるため、シート連続体60Cを吸収性本体連続体41Cに接合し易くすることができる。
また、工程S70では、湾曲したシート連続体60Cを吸収性本体連続体41Cと接合している。これにより、サイドシート62が着用者の身体の形状(具体的には、臀部と脚との境界線(肉割れ線))に沿って配置され易くなり、サイドシート62による違和感を着用者に与えにくくなる吸収性物品1を製造することができる。
加えて、シート連続体60Cを湾曲させることで、シート連続体60Cを湾曲させた後に、連続弾性部材CEを湾曲させながら配置する場合と比較して、連続弾性部材CEの位置を調整し易い。従って、狙い通りに連続弾性部材CEを湾曲させることができる。
また、シート連続体60Cを湾曲した後に本体接着剤71Cを塗布するケースでは、湾曲具合に合わせて本体接着剤71Cを塗布するには、高度な制御が必要である。工程S60では、本体接着剤71Cが塗布されたシート連続体60Cを湾曲している。従って、シート連続体60Cの湾曲に沿って本体接着剤71Cを塗布するための高度な制御が必要なくなり、本体接着剤を狙い通りの位置に塗布しやすくなる。
(4)変更例
次に、各変更例について、図10を用いて説明する。図10は、変更例に係る吸収性物品の模式断面図である。図10Aは、変更例1に係る吸収性物品1の模式断面図であり、図10Bは、変更例2に係る吸収性物品1の模式断面図である。図10における断面は、F4A-F4A断面に対応する。なお、実施形態と同様の説明は省略する。
次に、各変更例について、図10を用いて説明する。図10は、変更例に係る吸収性物品の模式断面図である。図10Aは、変更例1に係る吸収性物品1の模式断面図であり、図10Bは、変更例2に係る吸収性物品1の模式断面図である。図10における断面は、F4A-F4A断面に対応する。なお、実施形態と同様の説明は省略する。
変更例1について、図10Aを用いて説明する。図10Aに示すように、サイドシート62の端縁62Eは、立体ギャザー70に配置されている。この場合、サイドシート62の端縁62Eは、後述の立体ギャザー70の頂点Apを構成してよい。また、第2立体弾性部材752と起立端縁73との間の領域には、シート内接合部63が設けられていなくてもよい。すなわち、第2立体弾性部材752と起立端縁73との間の領域は、一対のシート層62pどうしが接合されていない内側非接合領域であってよい。これにより、一対のシート層62pの間に空間が発生するため、排泄物が、第2シート層622から第1シート層621へ連続的に染み込むことを抑制できる。
変更例2について、図10Bを用いて説明する。図10Bに示すように、第1シート層621が有する端縁62Eと第2シート層622が有する端縁62Eとが厚さ方向Tに重ならなくてよい。従って、第1シート層621が有する端縁62Eと第2シート層622が有する端縁62Eとが幅方向Wにずれていてよい。第1シート層621の端縁62Eと第2シート層622の端縁62Eとが、着用者の肌に一緒に当たり難くなり、肌触りの悪化を抑制することができる。第1シート層621の端縁62Eが、第2シート層622の端縁62Eよりも幅方向Wの外側に配置されていてもよく、第2シート層622の端縁62Eよりも幅方向Wの内側に配置されていてもよい。
変更例3について説明する。吸収性物品の製造方法は、工程S50の後に、シート連続体60Cを切断する工程を有してよい。シート連続体60Cを切断線CLに沿って切断することができる。次に、シート連続体60Cを切断した後に、切断によって製造された複合伸縮シート60を湾曲させる工程を行う。湾曲方法は、工程S60と同様である。
ここで、シート連続体60Cを湾曲させた場合、シート連続体60Cは搬送方向MDに連続しているため、シート連続体60Cには、交差方向CDの内側にかかる力と、交差方向CDの外側にかかる力とが交互に繰り返しかかり、シート連続体60Cを狙い通りに湾曲できない虞がある。そこで、複合伸縮シート60を個別に湾曲させることで、複合伸縮シート60を狙い通りに湾曲させることができる。
次に、湾曲した複合伸縮シート60を、工程S70と同様に、吸収性本体連続体41Cに接合する。これにより、狙い通りに湾曲させた複合伸縮シート60を吸収性本体連続体41Cに接合することができ、サイドシート62が着用者の身体の形状(具体的には、臀部と脚との境界線(肉割れ線))に沿ってさらに配置され易くなる。
(5)その他実施形態
以上、上述の実施形態を用いて本発明について詳細に説明したが、当業者にとっては、本発明が本明細書中に説明した実施形態に限定されるものではないということは明らかである。本発明は、特許請求の範囲の記載により定まる本発明の趣旨及び範囲を逸脱することなく修正及び変更態様として実施することができる。したがって、本明細書の記載は、例示説明を目的とするものであり、本発明に対して何ら制限的な意味を有するものではない。
以上、上述の実施形態を用いて本発明について詳細に説明したが、当業者にとっては、本発明が本明細書中に説明した実施形態に限定されるものではないということは明らかである。本発明は、特許請求の範囲の記載により定まる本発明の趣旨及び範囲を逸脱することなく修正及び変更態様として実施することができる。したがって、本明細書の記載は、例示説明を目的とするものであり、本発明に対して何ら制限的な意味を有するものではない。
上述において製造方法の工程の順番は、変更されてよい。例えば、工程S11は、工程S12の後に実行されてよい。また、上述において製造方法の一部の工程は省略されてよい。例えば、第1低伸縮領域LER1と第2低伸縮領域LER2を形成する工程の一方の工程は省略されてもよく、両方の工程が省略されてもよい。また、工程S20は省略されてもよい。上述の実施形態、各変更例及びその他実施形態に係る吸収性物品1に係る構成は、適宜組み合わせることが可能である。
なお、2019年6月20日に出願された日本国特許出願第2019-115024号の全内容が、参照により、本明細書に組み込まれる。
1:吸収性物品、15:外装体、16:ウエスト開口部、17:脚回り開口部、18:サイド接合部、20:前側外装体、30:後側外装体、40:本体部、41:吸収性本体、43:センターシート、46:液不透過シート、47:非肌面シート、48:非肌側サイドシート、50:吸収コア、60:複合伸縮シート、62:サイドシート、62p:シート層、63:シート内接合部、70:立体ギャザー、71:接合部、72:起立部、73:起立端縁、75:立体弾性部材、80:レッグギャザー、85:レッグ弾性部材、621:第1シート層、622:第2シート層、FL:第1折り目(1の折り目)、S1:前胴回り域、S2:後胴回り域、S3:股下域
Claims (18)
- 前後方向、前記前後方向に直交する幅方向、及び厚さ方向と、
前胴回り域と、後胴回り域と、前記前胴回り域及び前記後胴回り域に挟まれている股下域と、
吸収性物品の前記幅方向の中心よりも前記幅方向の外側に配置される1のサイドシートと、
立体ギャザーとレッグギャザーと、を有し、
前記立体ギャザーは、
前記前後方向に伸縮性を有する1以上の立体弾性部材によって起立可能である起立部と、
前記起立部の起立支点となる起立端縁と、を有し、
前記レッグギャザーは、前記前後方向に伸縮性を有する1以上のレッグ弾性部材によって所定の幅で前記前後方向に収縮する収縮領域を有し、かつ前記起立端縁よりも前記幅方向の外側に配置されている、吸収性物品であって、
前記立体ギャザーと前記レッグギャザーとは、前記1のサイドシートを前記前後方向に延びる1つの折り目を基点に折り返すことによって互いに対向する一対のシート層によって構成されており、
前記幅方向において、前記一対のシート層は、前記立体ギャザーの起立時に最も肌面側に位置する立体弾性部材と接する位置から、前記幅方向において最も外側に配置されているレッグ弾性部材と接する位置まで、連続的に延びている、吸収性物品。 - 前記1つの折り目が前記立体ギャザーに配置されるように、前記1のサイドシートが折り返されており、
前記1以上の立体弾性部材と前記1以上のレッグ弾性部材とが、前記一対のシート層に挟まれている請求項1に記載の吸収性物品。 - 前記1のサイドシートよりも非肌面側に配置され、かつ前記1のサイドシートと直接的又は間接的に接合される構成部材を有し、
前記構成部材は、前記起立端縁よりも前記幅方向の外側へ延びている請求項1又は2に記載の吸収性物品。 - 前記構成部材は、液不透過性を有する液不透過シートを有する、請求項3に記載の吸収性物品。
- 前記一対のシート層のそれぞれは、前記1のサイドシートの前記幅方向における端縁を有し、
前記一対のシート層の一方のシート層が有する前記端縁と他方のシート層が有する前記端縁とは、前記厚さ方向に重なっていない、請求項1から4のいずれか1項に記載の吸収性物品。 - 前記1以上のレッグ弾性部材の数は、前記1以上の立体弾性部材の数よりも多い、請求項1から5のいずれか1項に記載の吸収性物品。
- 前記1以上のレッグ弾性部材の数及び前記1以上の立体弾性部材の数は、2以上であり、
前記幅方向において、前記レッグ弾性部材どうしの間隔は、前記立体弾性部材どうしの間隔よりも狭い、請求項6に記載の吸収性物品。 - 前記立体ギャザーの起立時に最も非肌面側に位置する立体弾性部材と前記起立端縁との間において、接着剤により前記一対のシート層どうしを接合するシート内接合部を有する請求項1から7のいずれか1項に記載の吸収性物品。
- 前記立体ギャザーの起立時に最も非肌面側に位置する立体弾性部材と前記起立端縁との間の領域は、接着剤により前記一対のシート層どうしが接合されていない内側非接合領域である請求項1から7のいずれか1項に記載の吸収性物品。
- 前記幅方向において最も外側に配置されている前記レッグ弾性部材よりも前記幅方向の外側の領域は、前記一対のシート層どうしが接合されていない外側非接合領域である請求項1から9のいずれか1項に記載の吸収性物品。
- 前記吸収性物品の平面視において、前記1のサイドシートは、少なくとも前記吸収性物品の前記前後方向の中心よりも後側において、前記幅方向の外側へ向かうように湾曲しながら後方へ延びている部分を有する請求項1から10のいずれか1項に記載の吸収性物品。
- 吸収性物品の幅方向の中心よりも幅方向の外側に配置される1のサイドシートと、
立体ギャザーと、レッグギャザーと、を有し、
前記立体ギャザーは、
前後方向に伸縮性を有する1以上の立体弾性部材によって起立可能である起立部と、
前記起立部の起立支点となる起立端縁と、を有し、
前記レッグギャザーは、前記前後方向に伸縮性を有する1以上のレッグ弾性部材によって所定の幅で前記前後方向に収縮する収縮領域を有し、かつ前記起立端縁よりも前記幅方向の外側に配置されており、
前記立体ギャザーと前記レッグギャザーとは、前記1のサイドシートを前記前後方向に延びる1つの折り目を基点に折り返すことによって互いに対向する一対のシート層によって構成されている吸収性物品を製造する吸収性物品の製造方法であって、
前記一対のシート層を有しかつ伸縮性を有する複合伸縮シートが前記前後方向に連続したシート連続体を形成する形成工程を有し、
前記形成工程は、
前記1以上の立体弾性部材を構成する第1連続弾性部材及び前記1以上のレッグ弾性部材を構成する第2連続弾性部材からなる複数の連続弾性部材を、前記1のサイドシートが前記前後方向に連続したサイドシート連続体に配置する工程と、
前記複数の連続弾性部材の全てが前記サイドシート連続体に挟まれるように、前記サイドシート連続体を1回折り返す折り工程と、を有する、吸収性物品の製造方法。 - 前記形成工程は、前記第1連続弾性部材が配置される第1弾性領域と前記第2連続弾性部材が配置される第2弾性領域との間の中間領域に、前記サイドシート連続体どうしを接合する接着剤を塗布する工程をさらに有する請求項12に記載の吸収性物品の製造方法。
- 前記複合伸縮シートは、前記複合伸縮シートの前記前後方向の端部において、前記複合伸縮シートの前記前後方向の中央部よりも伸縮力が低い低伸縮領域を有しており、
前記シート連続体に、前記低伸縮領域を形成する工程と、
前記シート連続体を、少なくとも前記低伸縮領域と重なる領域において、前記1のサイドシートよりも非肌面側に配置される構成部材が連続した連続体と接合する工程と、を有する請求項12又は13に記載の吸収性物品の製造方法。 - 前記低伸縮領域を形成する工程では、前記シート連続体を圧搾して前記連続弾性部材を切断することにより、前記低伸縮領域を形成する請求項14に記載の吸収性物品の製造方法。
- 前記吸収性物品の平面視において、前記1のサイドシートが、少なくとも前記吸収性物品の前記前後方向の中心よりも後側において、前記幅方向の外側へ向かうように湾曲しながら後方へ延びている部分を有するように、前記シート連続体を湾曲する工程と、
湾曲した前記シート連続体を、前記1のサイドシートよりも非肌面側に配置される構成部材が連続した連続体と接合する工程と、を有する請求項12から15のいずれか1項に記載の吸収性物品の製造方法。 - 前記1のサイドシートよりも非肌面側に配置される構成部材が連続した連続体に前記シート連続体を接合するための本体接着剤を、前記シート連続体に塗布する工程を有し、
前記シート連続体を湾曲する工程では、前記本体接着剤が塗布された前記シート連続体を湾曲する請求項16に記載の吸収性物品の製造方法。 - 前記シート連続体を切断することによって前記複合伸縮シートを形成する工程と、
前記吸収性物品の平面視において、前記1のサイドシートが、少なくとも前記吸収性物品の前記前後方向の中心よりも後側において、前記幅方向の外側へ向かうように湾曲しながら後方へ延びている部分を有するように、前記複合伸縮シートを湾曲する工程と、
前記複合伸縮シートを、前記1のサイドシートよりも非肌面側に配置される構成部材が連続した連続体と接合する工程と、を有する請求項12から15のいずれか1項に記載の吸収性物品の製造方法。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202080045098.6A CN114080206B (zh) | 2019-06-20 | 2020-06-19 | 吸收性物品以及吸收性物品制造方法 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2019-115024 | 2019-06-20 | ||
| JP2019115024A JP7296260B2 (ja) | 2019-06-20 | 2019-06-20 | 吸収性物品 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2020256103A1 true WO2020256103A1 (ja) | 2020-12-24 |
Family
ID=73994461
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2020/024138 Ceased WO2020256103A1 (ja) | 2019-06-20 | 2020-06-19 | 吸収性物品、及び吸収性物品の製造方法 |
Country Status (3)
| Country | Link |
|---|---|
| JP (1) | JP7296260B2 (ja) |
| CN (1) | CN114080206B (ja) |
| WO (1) | WO2020256103A1 (ja) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115281939A (zh) * | 2022-09-06 | 2022-11-04 | 智邦(天津)卫生用品科技有限公司 | 卫生巾制备方法 |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2010088570A (ja) * | 2008-10-06 | 2010-04-22 | Kao Corp | 帯状材料の取付方法及び吸収性物品の製造方法 |
| JP2011523887A (ja) * | 2008-06-13 | 2011-08-25 | ザ プロクター アンド ギャンブル カンパニー | 液体排出物の封じ込めを改善するための弾性的に収縮可能なカフを有する使い捨て吸収性物品 |
| JP2015510838A (ja) * | 2012-03-30 | 2015-04-13 | ザ プロクター アンド ギャンブルカンパニー | 吸収性物品用レッグカフの製造方法及び製造装置 |
| JP2018511385A (ja) * | 2015-03-18 | 2018-04-26 | ザ プロクター アンド ギャンブル カンパニー | レッグカフを備える吸収性物品 |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3058918B1 (en) * | 2015-02-17 | 2019-04-17 | The Procter and Gamble Company | Absorbent articles forming a three-dimensional basin |
| JP6495765B2 (ja) * | 2015-06-30 | 2019-04-03 | ユニ・チャーム株式会社 | 使い捨ておむつ |
| JP6454658B2 (ja) * | 2016-03-30 | 2019-01-16 | 大王製紙株式会社 | 使い捨ておむつ |
| JP7456731B2 (ja) | 2019-05-30 | 2024-03-27 | 大王製紙株式会社 | 使い捨て着用物品 |
-
2019
- 2019-06-20 JP JP2019115024A patent/JP7296260B2/ja active Active
-
2020
- 2020-06-19 CN CN202080045098.6A patent/CN114080206B/zh active Active
- 2020-06-19 WO PCT/JP2020/024138 patent/WO2020256103A1/ja not_active Ceased
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2011523887A (ja) * | 2008-06-13 | 2011-08-25 | ザ プロクター アンド ギャンブル カンパニー | 液体排出物の封じ込めを改善するための弾性的に収縮可能なカフを有する使い捨て吸収性物品 |
| JP2010088570A (ja) * | 2008-10-06 | 2010-04-22 | Kao Corp | 帯状材料の取付方法及び吸収性物品の製造方法 |
| JP2015510838A (ja) * | 2012-03-30 | 2015-04-13 | ザ プロクター アンド ギャンブルカンパニー | 吸収性物品用レッグカフの製造方法及び製造装置 |
| JP2018511385A (ja) * | 2015-03-18 | 2018-04-26 | ザ プロクター アンド ギャンブル カンパニー | レッグカフを備える吸収性物品 |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115281939A (zh) * | 2022-09-06 | 2022-11-04 | 智邦(天津)卫生用品科技有限公司 | 卫生巾制备方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| CN114080206A (zh) | 2022-02-22 |
| CN114080206B (zh) | 2023-08-08 |
| JP2021000237A (ja) | 2021-01-07 |
| JP7296260B2 (ja) | 2023-06-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP4693530B2 (ja) | 使い捨ておむつ及びその製造方法 | |
| TW201103513A (en) | Pants type absorptive article and method of manufacturing same | |
| JP6752085B2 (ja) | 吸収性物品 | |
| WO2013005788A1 (ja) | パンツ型吸収性物品 | |
| JP2014069002A (ja) | 吸収性物品 | |
| CN109906066B (zh) | 一次性穿着物品及制造方法 | |
| JP6751625B2 (ja) | パンツ型吸収性物品 | |
| JP6042312B2 (ja) | 吸収性物品 | |
| JP2021000237A (ja) | 吸収性物品、及び吸収性物品の製造方法 | |
| KR20190045222A (ko) | 흡수성 물품 및 팬티형 흡수성 물품의 제조 방법 | |
| JP7083763B2 (ja) | 吸収性物品 | |
| JP7217148B2 (ja) | 吸収性物品 | |
| WO2019131110A1 (ja) | 吸収性物品 | |
| JP7349272B2 (ja) | 吸収性物品 | |
| JP5806846B2 (ja) | パンツ型吸収性物品 | |
| JP3241230U (ja) | 吸収性物品のパッケージ群 | |
| JP6412846B2 (ja) | 使い捨ておむつ | |
| JP7217203B2 (ja) | 吸収性物品 | |
| JP7848670B2 (ja) | 吸収性物品 | |
| JP7149070B2 (ja) | 吸収性物品 | |
| CN113226234B (zh) | 复合片、吸收性物品以及复合片的制造方法 | |
| JP7071146B2 (ja) | 使い捨て吸収性物品および使い捨て吸収性物品の製造方法 | |
| JPH08196567A (ja) | 立体パンツ型使いすておむつの製造方法 | |
| WO2023127549A1 (ja) | パンツ型吸収性物品、吸収性物品包装体、及び、パンツ型吸収性物品の製造方法 | |
| JP2023098678A (ja) | パンツ型吸収性物品、及び、吸収性物品包装体 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 20825609 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 20825609 Country of ref document: EP Kind code of ref document: A1 |