EP3526481B1 - Formschliesseinheit mit wärmemanagement - Google Patents
Formschliesseinheit mit wärmemanagement Download PDFInfo
- Publication number
- EP3526481B1 EP3526481B1 EP17783867.9A EP17783867A EP3526481B1 EP 3526481 B1 EP3526481 B1 EP 3526481B1 EP 17783867 A EP17783867 A EP 17783867A EP 3526481 B1 EP3526481 B1 EP 3526481B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cooling
- spindle
- bearing
- mould
- unit according
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/64—Mould opening, closing or clamping devices
- B29C45/66—Mould opening, closing or clamping devices mechanical
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/72—Heating or cooling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/83—Lubricating means
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16C—SHAFTS; FLEXIBLE SHAFTS; ELEMENTS OR CRANKSHAFT MECHANISMS; ROTARY BODIES OTHER THAN GEARING ELEMENTS; BEARINGS
- F16C19/00—Bearings with rolling contact, for exclusively rotary movement
- F16C19/22—Bearings with rolling contact, for exclusively rotary movement with bearing rollers essentially of the same size in one or more circular rows, e.g. needle bearings
- F16C19/34—Bearings with rolling contact, for exclusively rotary movement with bearing rollers essentially of the same size in one or more circular rows, e.g. needle bearings for both radial and axial load
- F16C19/38—Bearings with rolling contact, for exclusively rotary movement with bearing rollers essentially of the same size in one or more circular rows, e.g. needle bearings for both radial and axial load with two or more rows of rollers
- F16C19/383—Bearings with rolling contact, for exclusively rotary movement with bearing rollers essentially of the same size in one or more circular rows, e.g. needle bearings for both radial and axial load with two or more rows of rollers with tapered rollers, i.e. rollers having essentially the shape of a truncated cone
- F16C19/385—Bearings with rolling contact, for exclusively rotary movement with bearing rollers essentially of the same size in one or more circular rows, e.g. needle bearings for both radial and axial load with two or more rows of rollers with tapered rollers, i.e. rollers having essentially the shape of a truncated cone with two rows, i.e. double-row tapered roller bearings
- F16C19/386—Bearings with rolling contact, for exclusively rotary movement with bearing rollers essentially of the same size in one or more circular rows, e.g. needle bearings for both radial and axial load with two or more rows of rollers with tapered rollers, i.e. rollers having essentially the shape of a truncated cone with two rows, i.e. double-row tapered roller bearings in O-arrangement
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16C—SHAFTS; FLEXIBLE SHAFTS; ELEMENTS OR CRANKSHAFT MECHANISMS; ROTARY BODIES OTHER THAN GEARING ELEMENTS; BEARINGS
- F16C19/00—Bearings with rolling contact, for exclusively rotary movement
- F16C19/54—Systems consisting of a plurality of bearings with rolling friction
- F16C19/541—Systems consisting of juxtaposed rolling bearings including at least one angular contact bearing
- F16C19/542—Systems consisting of juxtaposed rolling bearings including at least one angular contact bearing with two rolling bearings with angular contact
- F16C19/543—Systems consisting of juxtaposed rolling bearings including at least one angular contact bearing with two rolling bearings with angular contact in O-arrangement
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16C—SHAFTS; FLEXIBLE SHAFTS; ELEMENTS OR CRANKSHAFT MECHANISMS; ROTARY BODIES OTHER THAN GEARING ELEMENTS; BEARINGS
- F16C37/00—Cooling of bearings
- F16C37/007—Cooling of bearings of rolling bearings
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C2045/1784—Component parts, details or accessories not otherwise provided for; Auxiliary operations not otherwise provided for
- B29C2045/1792—Machine parts driven by an electric motor, e.g. electric servomotor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/83—Lubricating means
- B29C2045/835—Lubricating means for ball screws or ball nuts
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/84—Safety devices
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16C—SHAFTS; FLEXIBLE SHAFTS; ELEMENTS OR CRANKSHAFT MECHANISMS; ROTARY BODIES OTHER THAN GEARING ELEMENTS; BEARINGS
- F16C2322/00—Apparatus used in shaping articles
Definitions
- the invention relates to a mold closing unit for injection molds on an injection molding machine for processing plastics and other plasticizable compounds, such as ceramic or powder compounds according to the preamble of claim 1.
- Injection molding machines or mold clamping units for injection molding machines with cooling concepts for heat or power dissipation are known in various ways.
- the need for a cooling concept arises from the high efficiency losses that are introduced into the system as heat, caused by an increase in friction due to the thermal growth of the individual elements, to protect the elements from increased wear and thermal overload.
- a spindle drive for an injection molding machine which has a lubricating area between the spindle and the spindle nut and a sealing area. At one end of the lubrication area there is a first lubricating oil seal which delimits the lubrication area and rests on the spindle. At the same end of the lubrication area, on the side of the first lubrication oil seal facing away from the lubrication area, there is a second lubrication oil seal resting on the spindle. The first seal keeps lubricating oil in the lubricating area.
- Cooled lubricating oil is fed into a lubricating area between the spindle and the spindle nut via a lubricating oil supply line within the spindle and a supply bore extending from there.
- No cooling element is provided for the spindle nut and there is no cooling path connected in series from the spindle via the spindle nut to the motor.
- the aim is targeted lubrication and lubricant removal from a drive spindle, whereby thermal aspects play no role.
- the DE 10 2006 024 712 A1 shows the use of several cooling circuits, but no series connection of cooling starting from a lance in a spindle via a cooling element on the spindle nut up to the motor in a serial cooling section.
- the EP 2 774 742 A1 describes in the relevant paragraphs (0036) to (0041) that the lubricant is fed from the ball screw nut to the ball screw spindle and is thrown out from there.
- a mold clamping unit with direct cooling of the bearing point of the spindle drive and / or one of the cooling plates assigned to the bearing points is known. Cooling channels penetrate the bearing point and / or the cooling plate assigned to the bearing point, so that the direct cooling results in a longer service life of the spindle system and a longer service life of the bearing.
- a mold clamping unit in which a liquid-cooled servomotor is used as a symmetrical drive and power transmission system.
- the servomotor drives a threaded spindle, which is non-rotatably connected to a cross head engaging the toggle lever system or systems. This results in a minimal size and it is possible to apply very high torques even at a standstill.
- the thermal energy dissipated by the electric servomotor by the water as a cooling medium can be recovered and then used, for example for mold temperature control.
- FIG DE 10 2012 108 061 A1 A preform for producing containers, in particular PET bottles, by means of stretch blow molding is shown in FIG DE 10 2012 108 061 A1 disclosed.
- the mold cavity consists of a cavity, a core, a neck ring, a support ring and a bottom insert.
- the bottom part has a substantially conical section and a sprue point arranged on the hollow cylinder axis, a connecting section with a curved outer wall being provided between the conical section and the sprue point.
- a feed channel is provided through which the cooling water enters the core can be directed. This is about cooling a mold cavity, but not about cooling mechanically interacting components.
- the present invention is based on the object of achieving more efficient cooling of the spindle unit.
- the mold clamping unit has at least one first, preferably stationary, mold carrier and one mold carrier that is movable relative to the first mold carrier and that together define a mold clamping space. Furthermore, a support element for an electromechanical closing mechanism is provided, which is actuated via at least one spindle unit and engages the movable mold carrier so that it can be moved cyclically or into an open position and a closed position with respect to an injection mold.
- the spindle unit has at least one spindle, at least one spindle nut which interacts with the spindle and which is attached in a bearing unit, and at least one motor which is attached in a bearing element.
- cooling elements penetrate at least the bearing unit and / or the bearing element with a cooling section in which the spindle and then the spindle nut are arranged.
- the spindle has at least one bore in the core, in which a cooling and / or lubricating medium is guided into the area of the contact points between the spindle nut and the spindle via at least one lance, whereby the amount of heat generated can be dissipated and efficient cooling of the spindle unit results.
- the cooling section is designed as a series connection for cooling the spindle via the lance, then the spindle nut via the cooling element and finally the motor.
- the invention can be applied not only to injection molding machines, but also to other machines which have at least one spindle unit.
- the bearing element encloses a storage space in which the storage unit is arranged and which is filled with the cooling and / or lubricating medium.
- the storage space is preferably a closed storage space in which cooling elements are provided, preferably in the form of a cooling coil, for cooling the lubricant. This results in a separation between the transmission medium as a cooling medium and the lubricating medium.
- the volume of the storage space makes it possible that there is advantageously sufficient cooling and / or lubricating medium for cooling and / or temperature control in the cooling section. Another advantage is that the bearing unit is lubricated, cooled and / or tempered at the same time.
- the cooling of the spindle, spindle nut, motor and at least one of the elements including the bearing unit or the bearing element is advantageously designed as a cooling path in parallel or in series, e.g. with the stipulation that the element with the highest power loss is supplied with the coolest cooling and / or lubricating medium .
- parallel connections of different cooling sections and / or individual cooling channels or combinations of series and parallel connections are also conceivable, so that an individual cooling concept tailored to the respective requirements can be created. Individual section cooling and combinations of those with parallel connections are also conceivable.
- cooling path as desired, for example from the outside to the inside, so that, for example, the coolest cooling and / or lubricating medium is not fed to the element with the highest power loss.
- the cooling path is also conceivable.
- the cooling section is preferably designed as a series connection of the elements from inside the spindle unit to the outside.
- the cooling section begins at the spindle and leads into the motor via the spindle nut and the cooling coil.
- a cascaded structure results in an optimal cooling concept, even for larger machines, in which, on the one hand, there is more heat, but on the other hand, due to the changed larger dimensions, it is more difficult to dissipate, especially inside a spindle drive.
- the spindle is the first part of the cooling section.
- the cooling prevents the spindle from growing thermally and damaging it. It is also conceivable that the cooling section is designed as a parallel connection or as a combination of series and parallel connection.
- the cooling and / or lubricating medium advantageously has oil. Any other medium that is capable of absorbing and releasing heat, for example water, and / or is suitable for lubrication is also conceivable.
- the spindle and the bearing unit are advantageously spatially separated, which leads to thermal decoupling and thus enables independent cooling or temperature control of the individual elements.
- the motor has an integrated thermal overload protection.
- the bearing unit is advantageously designed as a spherical roller thrust bearing. As a result, there are no dead spaces in which the cooling and / or lubricating medium can linger for a long time and thus clog the cooling path.
- other bearing units such as ball bearings, can also be used.
- the bearing unit is preferably designed at the same time as a conveying means that supports at least the conveyance of the cooling and / or lubricating medium.
- the spindle unit can advantageously be temperature-controlled in a targeted manner by means of the cooling and / or lubricating medium.
- the spindle unit is designed as a planetary roller screw drive, which is particularly advantageous for high precision and good power transmission properties with a comparatively high packing density.
- other power transmission units such as a ball screw drive or movement spindles of all kinds are also conceivable.
- the bearing element is advantageously designed as a separate element for simple assembly and is not integrated into the support element. Due to the local decoupling of the bearing element and the support element, advantageously no additional transverse forces act on the bearing element due to the deformation of the support element.
- the support element preferably has additional radial support means.
- the spindle nut and / or the storage space has at least one cooling coil in order to dissipate the heat energy that occurs.
- the cooling coil is preferably designed as a liquid cooler in a 2-circuit system.
- any other embodiment of the cooling coil and its arrangement for example as an external cooling arrangement or air / liquid cooling concepts, is also conceivable.
- a storage space cooled by the lubricating and / or cooling medium is advantageously provided, in which a lubricant is received for the interacting parts of the spindle unit. This enables thermal management with two different cooling circuits, which enables both good cooling and good cooling of the spindle unit at the same time.
- the lubricant can advantageously be circulated by a movement of the bearing unit in the storage space when the parts of the spindle unit interact, a homogeneous distribution of the lubricant in the storage space and thus heat distribution in this area between the spindle nut and spindle can be achieved.
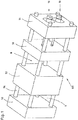
- Fig. 1 shows a perspective view obliquely from above of a mold clamping unit 100 for injection molds on an injection molding machine for processing plastics and other plasticizable masses such as ceramic or powdery masses with a first, preferably stationary mold carrier 50, a second movable mold carrier 52, which with the stationary mold carrier 50 one Defined mold clamping space R, and a closing mechanism M which engages on a support element 54 via a cross head 58 on the movable mold carrier 52.
- the mold clamping unit is in Fig. 1 assigned a plasticizing unit from the left, which is not shown in the drawing.
- an electromechanical closing mechanism M is provided, which is supported on the support element 54 and, in the exemplary embodiment, is designed as a toggle mechanism.
- Other drives such as spindle drives or hydraulic drives are just as conceivable as another support for the locking mechanism M, for example in a two-platen system in which one of the mold carriers 50, 52 also forms the support element, as long as an electromechanical locking mechanism is used.
- the closing mechanism By actuation of the closing mechanism, the movable mold carrier 52 moves towards and away from the stationary mold carrier 50.
- Support element 54, cross head 58, the movable mold carrier 52 and the stationary mold carrier 50 are connected to one another via bars 56.
- the locking mechanism M is preferably provided by at least one spindle unit 10, in the exemplary embodiment in FIG Fig. 1 by two spindle units 10 actuated.
- Fig. 2 shows the spindle unit 10 from Fig. 1 perspective from diagonally above. It has at least one spindle 12, at least one according to FIG Fig. 3 Spindle nut 14 cooperating with spindle 12 and mounted in a bearing unit 30 and at least one motor 18 mounted on a bearing element 16.
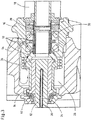
- a cooling with cooling elements such as cooling channels 32 or also the storage space 26 for dissipating heat from the spindle unit 10 penetrates according to FIG Fig. 3 and 4th at least the bearing unit 30 and / or the bearing element 16.
- cooling connections 22 for flanging on and / or connecting the cooling section or the cooling channels 32 are found according to FIG Fig. 2 at least on the lance 20, the bearing element 16 and the motor 18.
- the bearing element 16 encloses with the support element 54 a storage space 26 in which the bearing unit 30 is arranged and which is filled with the cooling and / or lubricating medium.
- the storage space 26 is preferably a closed or encapsulated storage space in which cooling elements are provided, preferably in the form of a cooling coil 36, for cooling the lubricant. This results in a separation between the transmission medium as a cooling medium and the lubricating medium.
- the support element 54 is designed in a preferred embodiment as a support plate or can be in a two-plate system e.g. be one of the mold carriers 50, 52.
- the cooling is carried out 18 as a cooling path in series for cooling the spindle 12, then the spindle nut 14 via the lance 20 and finally the motor 18 from inside the spindle unit 10 to the outside, with the proviso that the element with the highest power loss is the coolest cooling - and or To supply lubricant.
- at least one of the elements comprising the bearing unit 30 or bearing element 16 can be provided in the cooling section.
- the cooling path begins at the spindle 12 and leads via the spindle nut 14 and via the cooling coil 36 into the motor 18.
- the spindle 12, the oil space or storage space 26 and the motor are cooled one after the other. To do this, in Fig.
- Cooling connections 22 of the spindle 12 are connected to the cooling connections 22 of the bearing element 16 and of the motor 18 in this order, so that the coolest cooling and / or lubricating medium reaches the spindle 12 first.
- the flow direction in the motor 18 is irrelevant, so that a transfer of the cooling and / or lubricating medium from the bearing element 16 directly to the cooling connection 22 of the motor 18 is possible. Interfering edges and hose lines are advantageously minimized or eliminated.
- the cooling section is designed as a series connection, the spindle 12 being particularly preferably the first part of the cooling section. This ensures effective cooling of the spindle 12 within the cooling section.
- Oil is preferably used as the cooling and / or lubricating medium. Oil offers good properties with regard to the absorption and removal of thermal energy and can advantageously be used at the same time to lubricate elements of the spindle unit 10, for example the bearing unit 30. However, other cooling and / or lubricating media are also conceivable.
- the spindle 12 and the bearing unit 30 are preferably shown in FIG Fig. 3 and 4th spatially separated.
- the motor 18 drives the rotating element of the spindle 12 and spindle nut 14 via a drive shaft 28, the spindle nut 14 in the exemplary embodiment.
- the spatial separation means that the elements are thermally decoupled, and it is thus possible to cool or close the elements individually temper. In principle, however, the spatial separation of further elements of the spindle unit 10, such as the motor 18, is also conceivable.
- the motor 18 preferably has an integrated thermal overload protection as a protective safeguard for the cooling section. This advantageously ensures that if the temperature of the cooling section is too high, it is cooled or tempered by means of a cold cooling and / or lubricating medium. For example, if the temperature rises further, it is switched off, which protects against thermal overload.
- the bearing unit 30 is designed as a spherical roller thrust bearing.
- An optimal circulation of the cooling and / or lubricating medium in the storage space 26 is achieved by the conveying effect of the spherical roller bearing.
- the lubricating medium is encapsulated in the storage space 26 and conveyed through the storage unit 30, it can be cooled by the cooling coil 36 via the cooling medium. There are therefore no dead spaces in which the cooling and / or lubricating medium can linger for a long time and thus clog the cooling path.
- the spherical roller thrust bearing can thus at the same time be designed as a conveying means supporting at least the conveyance of the cooling and / or lubricating medium.
- other bearing units 30 are also conceivable, such as ball bearings, which can likewise be designed as conveying means.
- the cooling and / or lubricating medium it is preferably also possible to control the temperature of the spindle unit 10 in a targeted manner.
- the circulation of the cooling and / or lubricating medium is in the exemplary embodiment in Fig. 3 represented with the aid of arrows 64.
- the circulation of the lubricant located there and thus also the cooling is supported by the conveying effect of the bearing unit 30.
- the bearing unit 30 preferably has angular contact ball bearings which, when they move, preferably swirl the lubricant in the storage space.
- the cooling and / or lubricating medium flows through the cooling channels 32 and past the cooling coil 36. This creates a continuous circulation so that a homogeneous temperature distribution is established.
- the cooling coil 36 cools the cooling and / or lubricating medium in the storage space 26. Together, this brings about both lubrication and cooling of the spindle nut 14 and the bearing unit 30.
- the cooling of the cooling coil 36 is separate from the circulation of the cooling and / or lubricating medium in the storage space 26.
- a cooling and / or lubricating medium for cooling the cooling coil 36 water is used, for example, while the cooling and / or lubricating medium for the Circulation is e.g. oil.
- the first cooling circuit for example, water is used as a cooling and / or lubricating medium and cools the spindle 12 via the lance 20, then the spindle nut 14 and the storage space 26 via the cooling coil 36 and finally the motor 18.
- oil is used as Cooling and / or lubricating medium used.
- the oil circulates in the storage space 26 and is cooled by the cooling coil 36. In addition to this, in addition to cooling, the oil also lubricates the spindle nut 14 and the bearing unit 30. Both cooling circuits are preferably designed as, for example, a series and / or parallel connection.
- the cooling of the cooling coil 36 and the circulation in the storage space 26 are not separate from one another and, for example, oil is used as a common cooling and / or lubricating medium.
- oil is used as a common cooling and / or lubricating medium.
- the "cold" oil as a cooling and / or lubricating medium first cools the spindle 12 via the lance 20, then the spindle nut 14 via the cooling coil 36 and is then used for circulation in the storage space 26 and finally for cooling the motor 18th
- the cooling of the cooling coil 36 is in the cooling path between e.g. Integrated spindle 12 and motor 18.
- a cooling and / or lubricating medium e.g. Water provided.
- the cooling and / or lubricating medium is first applied with the aid of e.g. a series connection of the lance 20, then the cooling coil 36 and finally the motor 18. This results in a cooling path from the spindle 12 via the spindle nut 14 to the motor 18.
- the circulation of the cooling and / or lubricating medium, for example oil, in the storage space 26 is separate from the cooling path in this exemplary embodiment.
- the entire spindle unit 10 is preferably designed as a planetary roller screw drive, as a result of which the spindle unit 10 is characterized by high precision, good power transmission properties and a comparatively high packing density.
- the bearing element 16 is preferably designed as a separate element and not integrated into the support element 54 or not part of it. This results in simple assembly and, due to the decoupling between the bearing element 16 and the support element 54, no additional transverse forces due to the deformation of the support element 54 act on the bearing element 16.
- the support element 54 has in the exemplary embodiment Fig. 3 and 4th additional radial support means 62 for advantageous gravity compensation.
- the spindle nut 14 and / or the storage space 26 preferably has at least one cooling coil 36.
- the resulting amount of heat can thus advantageously be given off efficiently and the spindle nut 14 can be cooled and / or tempered.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
- Injection Moulding Of Plastics Or The Like (AREA)
- Producing Shaped Articles From Materials (AREA)
Description
- Die Erfindung betrifft eine Formschließeinheit für Spritzgießformen an einer Spritzgießmaschine zur Verarbeitung von Kunststoffen und anderer plastifizierbarer Massen, wie keramische oder pulverige Massen nach dem Oberbegriff des Anspruches 1.
- Spritzgießmaschinen bzw. Formschließeinheiten für Spritzgießmaschinen mit Kühlkonzepten für die Wärme- bzw. Leistungsabfuhr sind in unterschiedlicher Art bekannt. Die Notwendigkeit eines Kühlkonzeptes ergibt sich aus den hohen Wirkungsgradverlusten, die als Wärme, hervorgerufen durch eine Reibungserhöhung aufgrund des thermischen Wachsens der Einzelelemente, in das System eingebracht werden, zum Schutz der Elemente vor erhöhtem Verschleiß und thermischer Überlast.
- In der dem Oberbegriff des Anspruches 1 zugrunde liegenden
DE 10 2010 051 766 A1 ist ein Spindelantrieb für eine Spritzgießmaschine offenbart, welche einen Schmierbereich zwischen Spindel und Spindelmutter und einen Dichtbereich aufweist. An einem Ende des Schmierbereichs befindet sich eine erste Schmieröldichtung, welche den Schmierbereich begrenzt und an der Spindel anliegt. Am selben Ende des Schmierbereichs, an der schmierbereichabgewandten Seite der ersten Schmieröldichtung, befindet sich eine zweite an der Spindel anliegende Schmieröldichtung. Durch die erste Dichtung wird Schmieröl im Schmierbereich gehalten. Falls dennoch Schmieröl in den Dichtbereich eindringt, wird das Schmieröl von der zweiten Dichtung abgestreift, sodass das Schmieröl durch eine, zwischen den beiden Dichtungen angeordnete Austrittsöffnung, abfließen kann. Über eine Schmierölzuführleitung innerhalb der Spindel und einer von dort ausgehenden Zuführbohrung erfolgt die Zuführung von gekühltem Schmieröl in einen Schmierbereich zwischen Spindel und Spindelmutter. Für die Spindelmutter ist kein Kühlelement vorgesehen und eine Kühlstrecke in Reihenschaltung von Spindel über Spindelmutter zum Motor liegt dort nicht vor. Ziel ist eine gezielte Schmierung und Schmiermittelabfuhr an einer Antriebsspindel, wobei thermische Gesichtspunkte keine Rolle spielen. - Die
DE 10 2006 024 712 A1 zeigt die Verwendung mehrere Kühlkreisläufe, jedoch keine Reihenschaltung der Kühlung ausgehend von einer Lanze in einer Spindel über ein Kühlelement an der Spindelmutter bis hin zum Motor in einer seriellen Kühlstrecke. - Die
EP 2 774 742 A1 beschreibt in den relevanten Absätzen (0036) bis (0041, dass das Schmiermittel ausgehend von der Kugelrollmutter der Kugelrollspindel zugeführt wird und von dort verschleudert wird. Damit ist dort eine andere Reihenfolge der zu kühlenden Elemente gegeben. - Aus der
DE 10 2008 051 285 B3 ist eine Formschließeinheit mit einer direkten Kühlung der Lagerstelle des Spindelantriebes und/oder einer der Lagerstellen zugeordneten Kühlplatten bekannt. Kühlkanäle durchsetzen die Lagerstelle und/oder die der Lagerstelle zugeordnete Kühlplatte, so dass durch die unmittelbare Kühlung sich eine höhere Lebensdauer des Spindelsystems sowie eine höhere Lebensdauer der Lagerung ergeben. - Aus der
EP 0 658 136 B1 ist eine Formschließeinheit bekannt, in der ein flüssigkeitsgekühlter Servomotor als symmetrisches Antriebs- und Kraftübertragungssystem verwendet wird. Der Servomotor treibt eine Gewindespindel an, welche drehfest mit einem an dem oder den Kniehebelsystemen angreifenden Kreuzkopf verbunden ist. Dadurch ergibt sich eine minimale Baugröße und es ist möglich, auch im Stillstand sehr hohe Drehmomente aufzubringen. Die durch das Wasser als Kühlmedium vom elektrischen Servomotor abgeführte Wärmeenergie kann zurückgewonnen und anschließend, beispielsweise zur Werkzeugtemperierung, genutzt werden. - Ein Vorformling zur Herstellung von Behältern, insbesondere von PET-Flaschen, mittels Streckblasformen ist in der
DE 10 2012 108 061 A1 offenbart. Das Formnest besteht aus einer Kavität, einem Kern, einem Halsring, einem Stützring und einem Bodeneinsatz. Das Bodenteil weist einen im Wesentlichen konischen Abschnitt und einen an der Hohlzylinderachse angeordneten Angusspunkt auf, wobei zwischen dem konischen Abschnitt und dem Angusspunkt ein Verbindungsabschnitt mit gekrümmter Außenwand vorgesehen ist. Für eine möglichst schnelle Abkühlung der Formmasse innerhalb des Kerns ist ein Zuführkanal vorgesehen, durch den Kühlwasser in den Kern geleitet werden kann. Damit geht es hier um die Kühlung eines Formhohlraums, aber nicht um die Kühlung mechanisch zusammenwirkender Bauteile. - Dennoch ergibt sich auch bei diesen Lösungen nach dem Stand der Technik aufgrund der Wärmeentwicklung weiterhin ein thermisches Wachsen der Einzelkomponenten der Spindeleinheit, was zur Folge wiederum zu einer höheren Verlustleistung, hervorgerufen durch die Reibungserhöhung im Innern der Spindeleinheit, führt.
- Ausgehend von diesem Stand der Technik liegt der vorliegenden Erfindung die Aufgabe zugrunde, eine effizientere Kühlung der Spindeleinheit zu erreichen.
- Diese Aufgabe wird mit einer Formschließeinheit gemäß den Merkmalen des Anspruchs 1 gelöst. Vorteilhafte Weiterbildungen sind Gegenstand der abhängigen Ansprüche. Die in den Ansprüchen einzeln aufgeführten Merkmale sind in technologisch sinnvoller Weise miteinander kombinierbar und können durch erläuternde Sachverhalte aus der Beschreibung und durch Details aus den Figuren ergänzt werden, wobei weitere Ausführungsvarianten der Erfindung aufgezeigt werden.
- Die Formschließeinheit weist wenigstens einen ersten, vorzugsweise stationären Formträger und einen relativ zum ersten Formträger beweglichen Formträger auf, welche zusammen einen Formspannraum definieren. Ferner ist ein Abstützelement für einen elektromechanischen Schließmechanismus vorgesehen, welcher über wenigstens eine Spindeleinheit betätigt wird und an dem beweglichen Formträger angreift, sodass dieser zyklisch bewegt bzw. in eine Öffnungsposition und eine Schließposition bzgl. einer Spritzgießform gefahren werden kann. Die Spindeleinheit weist wenigstens eine Spindel, wenigstens eine mit der Spindel zusammenwirkende, in einer Lagereinheit angebrachte Spindelmutter und wenigstens einen in einem Lagerelement angebrachten Motor auf. Zur Kühlung durchdringen Kühlelemente wenigstens die Lagereinheit und/oder das Lagerelement mit einer Kühlstrecke, in der die Spindel und danach die Spindelmutter angeordnet ist. Dabei weist die Spindel im Kern wenigstens eine Bohrung auf, in welcher über wenigstens eine Lanze ein Kühlungs- und/oder Schmiermedium in den Bereich der Kontaktstellen zwischen der Spindelmutter und der Spindel geführt ist, wodurch sich die entstandene Wärmemenge abführen lässt und sich eine effiziente Kühlung der Spindeleinheit ergibt. Die Kühlstrecke ist als Reihenschaltung zur Kühlung der Spindel über die Lanze, danach der Spindelmutter über das Kühlelement und zuletzt des Motors ausgeführt. Prinzipiell lässt sich die Erfindung nicht nur auf Spritzgießmaschinen, sondern auch auf andere Maschinen übertragen, die wenigstens eine Spindeleinheit aufweisen.
- Das Lagerelement umschließt mit dem Abstützelement einen Lagerraum, in welchem die Lagereinheit angeordnet ist und der mit dem Kühlungs- und/oder Schmiermedium gefüllt ist. Vorzugsweise ist der Lagerraum ein geschlossener Lagerraum, in dem Kühlelemente vorzugsweis in Form einer Kühlwendel zur Kühlung des Schmiermittels vorgesehen sind. Dadurch erfolgt eine Trennung zwischen dem Übertragungsmedium als Kühlungsmedium und dem Schmiermedium. Durch das Volumen des Lagerraums ist es möglich, dass vorteilhaft ausreichend Kühlungs- und/oder Schmiermedium zur Kühlung und/oder Temperierung in der Kühlstrecke vorhanden ist. Ein weiterer Vorteil besteht darin, dass die Lagereinheit gleichzeitig geschmiert, gekühlt und/oder temperiert wird.
- Die Kühlung von Spindel, Spindelmutter, Motor sowie wenigstens einem der Elemente umfassend die Lagereinheit oder das Lagerelement ist vorteilhaft als eine Kühlstrecke in Parallel- oder Reihenschaltung ausgeführt, z.B. mit der Maßgabe dem Element mit der höchsten Verlustleistung das kühlste Kühlungs- und/oder Schmiermedium zuzuführen. Dadurch ergibt sich ein bedarfsorientiertes Wärmemanagement hinsichtlich einer zielgerichteten Kühlung und/oder Temperierung. Denkbar sind aber auch Parallelschaltungen von verschiedenen Kühlstrecken und/oder von einzelnen Kühlkanälen oder Kombinationen von Reihen- und Parallelschaltungen, sodass ein individuelles Kühlkonzept, zugeschnitten auf die jeweiligen Anforderungen, erstellt werden kann. Auch Einzelstreckenkühlungen und Kombinationen derer mit Parallelschaltungen sind denkbar. Es ist ebenso möglich, die Kühlstrecke beliebig auszuführen, z.B. von außen nach innen, sodass z.B. dem Element mit der höchsten Verlustleistung nicht das kühlste Kühlungs- und/oder Schmiermedium zugeführt wird. Denkbar ist aber auch jede beliebige andere Anordnung der Elemente in der Kühlstrecke.
- Vorzugsweise ist die Kühlstrecke als Reihenschaltung der Elemente von innerhalb der Spindeleinheit nach außen ausgebildet. Beispielsweise fängt die Kühlstrecke an der Spindel an und führt über die Spindelmutter sowie über die Kühlwendel in den Motor. So ergibt sich durch einen kaskadierten Aufbau ein optimales Kühlkonzept auch bei größeren Maschinen, bei denen die Wärme einerseits vermehrt anfällt, andererseits aber aufgrund der veränderten größeren Dimensionen gerade im Innern eines Spindelantriebs schwieriger abzuführen ist.
- Um für die Spindel eine effektive Kühlung zu gewährleisten, ist vorteilhaft die Spindel der erste Teil der Kühlstrecke ist. Durch die Kühlung wird verhindert, dass die Spindel thermisch wächst und es so zu Beschädigungen kommt. Ebenfalls denkbar ist auch, dass die Kühlstrecke als Parallelschaltung oder als eine Kombination von Reihen- und Parallelschaltung ausgeführt ist.
- Vorteilhaft weist das Kühlungs- und/oder Schmiermedium Öl auf. Denkbar ist aber auch jedes andere Medium, welches in der Lage ist, Wärme aufzunehmen und abzugeben, beispielsweise Wasser, und/oder zum Schmieren geeignet ist.
- Für ein bedarfsgerechtes Wärmemanagement der einzelnen Elemente sind vorteilhaft die Spindel und die Lagereinheit räumlich getrennt, was zu einer thermischen Entkopplung führt, und so eine unabhängige Kühlung bzw. Temperierung der einzelnen Elemente möglich macht.
- Für eine vorteilhafte zusätzliche Schutzabsicherung der Kühlstrecke weist der Motor eine integrierte thermische Überlastsicherung auf.
- Zur Aufnahme hoher axialer Belastungen und für eine optimale Zirkulation des Kühlungs- und/oder Schmiermediums aufgrund des Fördereffekts ist die Lagereinheit vorteilhaft als ein Axial-Pendelrollenlager ausgeführt. Es ergeben sich dadurch keine Toträume, in denen das Kühlungs- und/oder Schmiermedium langfristig verweilen kann und somit die Kühlstrecke verstopfen kann. Prinzipiell sind aber auch andere Lagereinheiten, wie z.B. Kugellager verwendbar.
- Vorzugsweise ist die Lagereinheit zugleich als ein zumindest die Förderung des Kühlungs- und/oder Schmiermediums unterstützendes Fördermittel ausgebildet.
- Für eine extrem hohe Genauigkeit, kann neben der normalen Kühlung, vorteilhaft die Spindeleinheit mittels des Kühlungs- und/oder Schmiermediums gezielt temperiert werden.
- Besonders vorteilhaft für eine hohe Präzision und gute Kraftübertragungseigenschaften bei vergleichsweise hoher Packungsdichte ist die Spindeleinheit als ein Planetenrollengewindetrieb ausgeführt. Denkbar sind aber auch andere Kraftübertragungseinheiten wie beispielsweise ein Kugelgewindetrieb oder Bewegungsspindeln aller Art.
- Das Lagerelement ist für eine einfache Montage vorteilhaft als ein gesondertes Element ausgeführt und ist nicht in das Abstützelement integriert. Aufgrund der örtlichen Entkopplung von Lagerelement und Abstützelement wirken vorteilhaft keine zusätzlichen Querkräfte durch die Verformung des Abstützelements auf das Lagerelement.
- Zusätzlich zur Schwerkraftkompensation hinsichtlich einer guten Arretierung der Spindel weist das Abstützelement vorzugsweise zusätzliche radiale Abstützmittel auf.
- Es ist von Vorteil, wenn die Spindelmutter und/oder der Lagerraum zur Abführung von entstehender Wärmeenergie wenigstens eine Kühlwendel aufweist. Die Kühlwendel ist vorzugsweise als ein Flüssigkeitskühler in einem 2-Kreissystem ausgeführt. Denkbar ist aber auch jede andere Ausführungsform der Kühlwendel und deren Anordnung beispielsweise als eine externe Kühlanordnung oder Luft-/Flüssig-keitskühlkonzepte.
- Vorteilhaft ist ein vom Schmier- und/oder Kühlmedium gekühlter Lagerraum vorgesehen ist, in dem ein Schmiermittel für die zusammenwirkenden Teile der Spindeleinheit aufgenommen ist. Damit ist ein Wärmemanagement mit zwei unterschiedlichen Kühlkreisläufen möglich, der zugleich eine gute Kühlung als auch gute Kühlung der Spindeleinheit ermöglicht.
- Ist zudem vorteilhaft das Schmiermittel durch eine beim Zusammenspiel der Teile der Spindeleinheit erfolgende Bewegung der Lagereinheit im Lagerraum umwälzbar, kann eine homogene Verteilung des Schmiermittels im Lagerraum und damit Wärmeverteilung in diesem Bereich zwischen Spindelmutter und Spindel erreicht werden.
- Weitere Vorteile ergeben sich aus den Unteransprüchen und der nachfolgenden Beschreibung eines bevorzugten Ausführungsbeispiels. Die in den Patentansprüchen einzeln aufgeführten Merkmale sind in technologisch sinnvoller Weise miteinander kombinierbar und können durch erläuternde Sachverhalte aus der Beschreibung und durch Details aus den Figuren ergänzt werden, wobei weitere Ausführungsvarianten der Erfindung aufgezeigt werden.
- Im Folgenden wird die Erfindung anhand eines in den beigefügten Figuren dargestellten Ausführungsbeispiels näher erläutert. Es zeigen:
- Fig. 1
- eine perspektivische Ansicht von schräg oben einer Formschließeinheit mit zwei Spindeleinheiten,
- Fig. 2
- eine perspektivische Ansicht von schräg oben der Spindeleinheit gemäß
Fig. 1 , - Fig. 3
- eine Schnittansicht von der Seite eines Teils der Spindeleinheit mit Teilen der Formschließeinheit und eingezeichneter Zirkulation des Kühlungs- und/oder Schmiermediums,
- Fig. 4
- eine Schnittansicht von oben der Spindeleinheit mit Teilen der Formschließeinheit.
- Die Erfindung wird jetzt beispielhaft unter Bezug auf die beigefügten Zeichnungen näher erläutert. Allerdings handelt es sich bei den Ausführungsbeispielen nur um Beispiele, die nicht das erfinderische Konzept auf eine bestimmte Anordnung beschränken sollen. Bevor die Erfindung im Detail beschrieben wird, ist darauf hinzuweisen, dass sie nicht auf die jeweiligen Bauteile der Vorrichtung sowie die jeweiligen Verfahrensschritte beschränkt ist, da diese Bauteile und Verfahren variieren können. Die hier verwendeten Begriffe sind lediglich dafür bestimmt, besondere Ausführungsformen zu beschreiben und werden nicht einschränkend verwendet. Wenn zudem in der Beschreibung oder in den Ansprüchen die Einzahl oder unbestimmte Artikel verwendet werden, bezieht sich dies auch auf die Mehrzahl dieser Elemente, solange nicht der Gesamtzusammenhang eindeutig etwas Anderes deutlich macht.
-
Fig. 1 zeigt eine perspektivische Ansicht von schräg oben einer Formschließeinheit 100 für Spritzgießformen an einer Spritzgießmaschine zur Verarbeitung von Kunststoffen und anderen plastifizierbaren Massen wie keramischen oder pulvrigen Massen mit einem ersten, vorzugsweise stationären Formträger 50, einem zweiten beweglichen Formträger 52, welcher mit dem stationären Formträger 50 einen Formspannraum R definiert, und einem Schließmechanismus M, welcher an einem Abstützelement 54 über einen Kreuzkopf 58 an dem beweglichen Formträger 52 angreift. Üblicherweise ist der Formschließeinheit inFig. 1 von der linken Seite her eine Plastifiziereinheit zugeordnet, die zeichnerisch nicht dargestellt ist. - Für ein zyklisches Öffnen und Schließen der Spritzgießform ist ein elektromechanischer Schließmechanismus M vorgesehen, der sich an dem Abstützelement 54 abstützt, und im Ausführungsbeispiel als Kniehebelmechanismus ausgebildet ist. Andere Antriebe wie beispielsweise Spindelantriebe oder hydraulische Antriebe sind ebenso denkbar wie eine andere Abstützung des Schließmechanismus M z.B. in einem Zweiplattensystem, in dem einer der Formträger 50, 52 zugleich das Abstützelement bildet, so lange ein elektromechanischer Schließmechanismus verwendet wird. Durch Betätigung des Schließmechanismus bewegt sich der bewegliche Formträger 52 auf den stationären Formträger 50 zu und von diesem weg. Abstützelement 54, Kreuzkopf 58, der bewegliche Formträger 52 und der stationäre Formträger 50 sind über Holme 56 miteinander verbunden. Diese Holme 56 können - müssen aber nicht - gleichzeitig dem beweglichen Formträger 52 als Führung dienen. Alternativ können auch andere Kraftübertragungselement vorgesehen sein, die z.B. die Kräfte um den Aufspannraum R herumleiten. Vorzugsweise wird der Schließmechanismus M durch wenigstens eine Spindeleinheit 10, im Ausführungsbeispiel in
Fig. 1 durch zwei Spindeleinheiten 10, betätigt. -
Fig. 2 zeigt die Spindeleinheit 10 ausFig. 1 perspektivisch von schräg oben. Sie weist wenigstens eine Spindel 12, wenigstens eine gemäßFig. 3 mit der Spindel 12 zusammenwirkende und in einer Lagereinheit 30 angebrachte Spindelmutter 14 und wenigstens einen an einem Lagerelement 16 angebrachten Motor 18 auf. Eine Kühlung mit Kühlelementen wie Kühlkanälen 32 oder auch dem Lagerraum 26 zur Ableitung von Wärme aus der Spindeleinheit 10 durchdringt gemäßFig. 3 und4 wenigstens die Lagereinheit 30 und/oder das Lagerelement 16. Prinzipiell denkbar sind aber auch weitere Kühlkanäle 32 durch die Spindeleinheit 10, z.B. durch den Motor 18. Im Ausführungsbeispiel weist die Spindel 12 im Kern wenigstens eine Bohrung 24 auf, in welcher über wenigstens eine Lanze 20 ein Kühlungs- und/oder Schmiermedium in den Bereich der Kontaktstellen zwischen der Spindelmutter 14 und der Spindel 12 geführt ist, wodurch sich vorteilhaft eine effiziente Kühlung der Spindeleinheit 10 ergibt. Kühlanschlüsse 22 zum Anflanschen und/oder Verbinden der Kühlstrecke bzw. der Kühlkanäle 32 finden sich gemäßFig. 2 wenigstens an der Lanze 20, dem Lagerelement 16 und dem Motor 18. - In einem weiteren bevorzugten Ausführungsbeispiel gemäß
Fig. 3 und4 umschließt das Lagerelement 16 mit dem Abstützelement 54 einen Lagerraum 26, in welchem die Lagereinheit 30 angeordnet ist und der mit dem Kühlungs- und/oder Schmiermedium gefüllt ist. Vorzugsweise handelt es sich bei dem Lagerraum 26 um einen geschlossenen oder gekapselten Lagerraum, in dem Kühlelemente vorzugsweise in Form einer Kühlwendel 36 zur Kühlung des Schmiermittels vorgesehen sind. Dadurch erfolgt eine Trennung zwischen dem Übertragungsmedium als Kühlungsmedium und dem Schmiermedium. - Das Abstützelement 54 ist in einem bevorzugten Ausführungsbeispiel als eine Abstützplatte ausgeführt oder kann in einem Zweiplattensystem z.B. einer der Formträger 50, 52 sein.
- Die Kühlung ist 18 als eine Kühlstrecke in Reihenschaltung zur Kühlung der Spindel 12, danach der Spindelmutter 14 über die Lanze 20 und zuletzt des Motors 18 von innerhalb der Spindeleinheit 10 nach außen ausgeführt, mit der Maßgabe vorzugsweise dem Element mit der höchsten Verlustleistung das kühlste Kühlungs- und/oder Schmiermedium zuzuführen. Zudem kann in der Kühlstrecke wenigstens eines der Elemente umfassend die Lagereinheit 30 oder Lagerelement 16 vorgesehen sein. Beispielsweise fängt die Kühlstrecke an der Spindel 12 an und führt über die Spindelmutter 14 sowie über die Kühlwendel 36 in den Motor 18. Somit werden also nacheinander die Spindel 12, der Ölraum bzw. Lagerraum 26 und der Motor gekühlt. Dazu werden in
Fig. 2 Kühlanschlüsse 22 der Spindel 12 mit den Kühlanschlüssen 22 des Lagerelements 16 und des Motors 18 in dieser Reihenfolge verbunden, sodass das kühlste Kühlungs- und/oder Schmiermedium zuerst die Spindel 12 erreicht. Die Durchflussrichtung im Motor 18 ist dabei unerheblich, sodass eine Übergabe des Kühlungs- und/oder Schmiermedium von dem Lagerelement 16 direkt an den Kühlanschluss 22 des Motors 18 möglich ist. Vorteilhaft werden dadurch Störkanten und Schlauchleitungen minimiert bzw. eliminiert. Es ist ebenso möglich, die Kühlstrecke beliebig auszuführen, z.B. von außen nach innen, sodass z.B. dem Element mit der höchsten Verlustleistung nicht das kühlste Kühlungs- und/oder Schmiermedium zugeführt wird. Denkbar ist aber auch jede beliebige andere Anordnung der Elemente in der Kühlstrecke. - Prinzipiell denkbar sind neben einer Reihenschaltung auch Parallelschaltungen und/oder eine Kombination aus Reihen- und Parallelschaltung. Vorteilhaft können mit einer Parallelschaltung einzelne und/oder alle Kühlkanäle der einzelnen Elemente der Spindeleinheit 10 einzeln angesteuert und unabhängig voneinander gekühlt und/oder temperiert werden. Auch eine Einzelstreckenkühlung oder eine Kombination zwischen Einzelstreckenkühlung und Parallelschaltung der Kühlkanäle 32 ist denkbar.
- Im Ausführungsbeispiel ist die Kühlstrecke als Reihenschaltung ausgeführt, wobei besonders bevorzugt die Spindel 12 der erste Teil der Kühlstrecke ist. Dadurch wird eine effektive Kühlung der Spindel 12 innerhalb der Kühlstrecke gewährleistet.
- Als Kühlungs- und/oder Schmiermedium wird vorzugsweise Öl verwendet. Öl bietet gute Eigenschaften hinsichtlich der Aufnahme und Abfuhr von Wärmeenergie und kann vorteilhaft gleichzeitig zum Schmieren von Elementen der Spindeleinheit 10, beispielsweise der Lagereinheit 30, verwendet werden. Denkbar sind jedoch auch andere Kühlungs- und/oder Schmiermedien.
- Um ein bedarfsgerechtes Wärmemanagement der einzelnen Komponenten der Spindeleinheit 10 zu realisieren, sind vorzugsweise die Spindel 12 und die Lagereinheit 30 gemäß
Fig. 3 und4 räumlich getrennt. Ferner treibt der Motor 18 über eine Antriebswelle 28 das drehende Element von Spindel 12 und Spindelmutter 14 an, im Ausführungsbeispiel die Spindelmutter 14. Durch die räumliche Trennung sind die Elemente thermisch entkoppelt, und es ist somit möglich, die Elemente einzeln zu kühlen bzw. zu temperieren. Prinzipiell denkbar ist aber auch die räumliche Trennung weiterer Elemente der Spindeleinheit 10 wie z.B. des Motors 18. - Vorzugsweise weist der Motor 18 eine integrierte thermische Überlastsicherung als eine Schutzabsicherung der Kühlstrecke auf. Dadurch wird vorteilhaft erreicht, dass im Falle einer zu hohen Temperatur der Kühlstrecke, diese mittels kaltem Kühlungs- und/oder Schmiermedium abgekühlt bzw. temperiert wird. Beispielsweise erfolgt bei weiterer Temperaturerhöhung eine Abschaltung, welche vor thermischer Überlast schützt.
- Im Ausführungsbeispiel gemäß
Fig. 3 und4 ist die Lagereinheit 30 als ein Axial-Pendelrollenlager ausgeführt. Durch die Förderwirkung des Pendelrollenlagers wird eine optimale Zirkulation des Kühlungs- und/oder Schmiermediums in dem Lagerraum 26 erreicht. Vorzugsweise erfolgt dabei eine Trennung zwischen Kühl- und Schmiermedium. Während das Schmiermedium im Lagerraum 26 gekapselt aufgenommen und durch die Lagereinheit 30 gefördert wird, kann es über das Kühlmedium durch die Kühlwendel 36 gekühlt werden. Es entstehen somit keine Toträume, in denen das Kühlungs- und/oder Schmiermedium lange verweilen kann, und so die Kühlstrecke verstopft. Das Axial-Pendelrollenlager kann also zugleich als ein zumindest die Förderung des Kühlungs- und/oder Schmiermedium unterstützendes Fördermittel ausgebildet sein. Prinzipiell denkbar sind aber auch andere Lagereinheiten 30, wie z.B. Kugellager, die ebenfalls als Fördermittel ausgebildet sein können. Mit dem Kühlungs- und/oder Schmiermedium ist es vorzugsweise auch möglich, die Spindeleinheit 10 gezielt zu temperieren. - Die Zirkulation des Kühlungs- und/oder Schmiermediums ist im Ausführungsbeispiel in
Fig. 3 mit Hilfe von Pfeilen 64 dargestellt. Im vorzugsweise gekapselten Lagerraum 26 wird die Zirkulation des dort befindlichen Schmiermittels und damit auch die Kühlung durch die Förderwirkung der Lagereinheit 30 unterstützt. Die Lagereinheit 30 weist dazu vorzugsweise Schrägkugellager auf, die bei ihrer Bewegung das Schmiermedium im Lagerraum vorzugsweise verwirbeln. Das Kühlungs- und/oder Schmiermedium fließt dabei durch die Kühlkanäle 32 und an der Kühlwendel 36 vorbei. Es entsteht so eine kontinuierliche Umwälzung, sodass sich eine homogene Temperaturverteilung einstellt. Ferner entstehen - unterstützt auch durch die Förderwirkung der Lagereinheit 30 - keine Toträume, in denen das Kühlungs- und/oder Schmiermedium verweilen kann. Weiterhin wird durch die Kühlwendel 36 das Kühlungs- und/oder Schmiermedium im Lagerraum 26 gekühlt. Zusammen bewirkt dies eine Schmierung als auch eine Kühlung der Spindelmutter 14 und der Lagereinheit 30. - Im Ausführungsbeispiel in
Fig. 3 ist die Kühlung der Kühlwendel 36 getrennt von der Zirkulation des Kühlungs- und/oder Schmiermediums im Lagerraum 26. Als Kühlungs- und/oder Schmiermedium für die Kühlung der Kühlwendel 36 wird z.B. Wasser verwendet, während hingegen das Kühlungs- und/oder Schmiermedium für die Zirkulation z.B. Öl ist. In diesem Fall ergeben sich wenigstens zwei voneinander getrennte Kühlkreisläufe. Im ersten Kühlkreislauf wird z.B. Wasser als Kühlungs- und/oder Schmiermedium verwendet und kühlt über die Lanze 20 die Spindel 12, danach über die Kühlwendel 36 die Spindelmutter 14 und den Lagerraum 26 und zuletzt den Motor 18. Für den zweiten Kühlkreislauf wird z.B. Öl als Kühlungs- und/oder Schmiermedium benutzt. Das Öl zirkuliert im Lagerraum 26 und wird von der Kühlwendel 36 gekühlt. Zusätzlich dazu bewirkt das Öl neben der Kühlung auch eine Schmierung der Spindelmutter 14 und der Lagereinheit 30. Beide Kühlkreisläufe sind bevorzugt als beispielsweise eine Reihen- und/oder Parallelschaltung ausgeführt. - Prinzipiell denkbar ist aber auch, dass alternativ die Kühlung der Kühlwendel 36 und die Zirkulation im Lagerraum 26 nicht getrennt voneinander sind und als gemeinsames Kühlungs- und/oder Schmiermedium z.B. Öl verwendet wird. Es existiert in diesem Fall lediglich ein Kühlkreislauf. Beispielsweise kühlt dann das "kalte" Öl als Kühlungs- und/oder Schmiermedium zuerst über die Lanze 20 die Spindel 12, danach über die Kühlwendel 36 die Spindelmutter 14 und wird danach für die Zirkulation im Lagerraum 26 verwendet und zum Schluss für die Kühlung des Motors 18.
- In einem besonders bevorzugten Ausführungsbeispiel ist die Kühlung der Kühlwendel 36 in die Kühlstrecke zwischen z.B. Spindel 12 und Motor 18 integriert. Als Kühlungs- und/oder Schmiermedium ist z.B. Wasser vorgesehen. Beispielsweise wird das Kühlungs- und/oder Schmiermedium zuerst mit Hilfe z.B. einer Reihenschaltung der Lanze 20, danach der Kühlwendel 36 und zuletzt dem Motor 18 zugeführt. Somit ergibt sich eine Kühlstrecke von der Spindel 12 über die Spindelmutter 14 bis hin zum Motor 18. Die Zirkulation des Kühlungs- und/oder Schmiermediums, beispielsweise Öl, im Lagerraum 26 ist in diesem Ausführungsbeispiel getrennt von der Kühlstrecke.
- Den verschiedenen Kühlstrecken ist damit gemeinsam, dass zielgerichtet eine systemisch als auch thermisch optimale und an die jeweiligen Bedürfnisse anpassbare Wärmeabführung von verschiedenen Wärmequellen erfolgt.
- Die gesamte Spindeleinheit 10 ist vorzugsweise als ein Planetenrollengewindetrieb ausgeführt, wodurch eine hohe Präzision, gute Kraftübertragungseigenschaften bei vergleichsweise hoher Packungsdichte die Spindeleinheit 10 charakterisieren.
- Gemäß
Fig. 3 und4 ist das Lagerelement 16 vorzugsweise als ein gesondertes Element ausgeführt und nicht in das Abstützelement 54 integriert bzw. kein Bestandteil davon. Dadurch ergibt sich eine einfache Montage und es wirken aufgrund der Entkopplung zwischen Lagerelement 16 und Abstützelement 54 keine zusätzlichen Querkräfte durch die Verformung des Abstützelements 54 auf das Lagerelement 16. - Das Abstützelement 54 weist im Ausführungsbeispiel der
Fig. 3 und4 zusätzliche radiale Abstützmittel 62 zur vorteilhaften Schwerkraftkompensation auf. - Vorzugsweise weist die Spindelmutter 14 und/oder der Lagerraum 26 wenigstens eine Kühlwendel 36 auf. Somit kann vorteilhaft die entstehende Wärmemenge effizient abgegeben und die Spindelmutter 14 gekühlt und/oder temperiert werden.
- Wenn im Rahmen dieser Anmeldung von Temperierung die Rede ist, so umfasst dies auch grundsätzlich eine Kühlung. In der Regel wird auch eine Kühlung erfolgen.
-
- 10
- Spindeleinheit
- 12
- Spindel
- 14
- Spindelmutter
- 16
- Lagerelement
- 18
- Motor
- 20
- Lanze
- 22
- Kühlanschlüsse
- 24
- Bohrung
- 26
- Lagerraum
- 28
- Antriebswelle
- 30
- Lagereinheit
- 32
- Kühlkanäle
- 36
- Kühlwendel
- 50
- erster, stationärer Formträger
- 52
- beweglicher Formträger
- 54
- Abstützelement
- 56
- Holme
- 58
- Kreuzkopf
- 62
- Abstützmittel
- 64
- Pfeil
- 100
- Formschließeinheit
- R
- Formspannraum
- M
- Schließmechanismus
Claims (15)
- Formschließeinheit (100) für Spritzgießformen an einer Spritzgießmaschine zur Verarbeitung von Kunststoffen und anderer plastifizierbarer Massen, wie keramische oder pulverige Massen, mit- wenigstens einem ersten, vorzugsweise stationären Formträger (50)- wenigstens einem relativ zum ersten Formträger beweglichen Formträger (52), der gemeinsam mit dem ersten Formträger (50) einen Formspannraum (R) zur Aufnahme einer Spritzgießform zwischen den beiden Formträgern ausbildet,- wenigstens einem Abstützelement (54) für wenigstens einen elektromechanischen Schließmechanismus (M) zum zyklischen Öffnen und Schließen der Spritzgießform unter Bewegung des beweglichen Formträgers (52) auf den ersten Formträger (50) zu und von diesem weg,- wobei der Schließmechanismus (M) durch wenigstens eine Spindeleinheit (10) betätigt wird, welche wenigstens eine Spindel (12), wenigstens eine mit der Spindel (12) zusammenwirkende, in einer Lagereinheit (30) angebrachte Spindelmutter (14) und wenigstens einen, an einem Lagerelement (16) angebrachten Motor (18) aufweist,- einer Kühlung mit Kühlelementen (36,32) zur Ableitung von Wärme aus der Spindeleinheit (10), wobei die Kühlelemente (36, 32) wenigstens die Lagereinheit (30) und/oder das Lagerelement (16) mit einer Kühlstrecke durchsetzen, in der die Spindel (12) und danach die Spindelmutter (14) angeordnet istwobei die Spindel (12) im Kern wenigstens eine Bohrung (24) aufweist, in welcher über wenigstens eine Lanze (20) ein Kühlungs- und/oder Schmiermedium in den Bereich der Kontaktstellen zwischen der Spindelmutter (14) und der Spindel (12) geführt ist,
dadurch gekennzeichnet, dass die Kühlstrecke als Reihenschaltung zur Kühlung der Spindel (12) über die Lanze (20), danach der Spindelmutter (14) über das Kühlelement (36) und zuletzt des Motors (18) ausgebildet ist. - Formschließeinheit nach Anspruch 1, dadurch gekennzeichnet, dass das Lagerelement (16) mit dem Abstützelement (54) einen Lagerraum (26) umschließt, in dem die Lagereinheit (30) angeordnet ist und der mit dem Kühlungs- und/oder Schmiermedium gefüllt ist.
- Formschließeinheit nach Anspruch 2, dadurch gekennzeichnet, dass der Lagerraum (26) ein geschlossener Lagerraum ist, in dem Kühlelemente (36, 32) vorzugsweise in Form einer Kühlwendel (36) zur Kühlung des Schmiermittels vorgesehen sind.
- Formschließeinheit nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Kühlung von Spindel (12), Spindelmutter (14), Motor (18) sowie von wenigstens einem der Elemente umfassend die Lagereinheit (30) oder das Lagerelement (16) als eine Kühlstrecke in Parallel- oder Reihenschaltung ausgebildet ist, vorzugsweise mit der Maßgabe dem Element mit der höchsten Verlustleistung das kühlste Kühlungs- und/oder Schmiermedium zuzuführen.
- Formschließeinheit nach Anspruch 4, dadurch gekennzeichnet, dass die Kühlstrecke als Reihenschaltung der Elemente von innerhalb der Spindeleinheit nach außen ausgebildet ist.
- Formschließeinheit nach Anspruch 4 oder 5, dadurch gekennzeichnet, dass die Spindel (12) der erste Teil der Kühlstrecke ist.
- Formschließeinheit nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Spindel (12) und die Lagereinheit (30) räumlich getrennt sind.
- Formschließeinheit nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass der Motor (18) eine integrierte thermische Überlastsicherung aufweist, die vorzugsweise bei weiterer Temperaturerhöhung eine Abschaltung zur Absicherung vor weiterer thermischer Überlast herbeiführt.
- Formschließeinheit nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Lagereinheit (30) als ein Axial-Pendelrollenlager ausgeführt ist und/oder zugleich als ein zumindest die Förderung des Kühlungs- und/oder Schmiermedium unterstützendes Fördermittel ausgebildet ist.
- Formschließeinheit nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Spindeleinheit (10) mittels des Kühlungs- und/oder Schmiermediums gezielt temperierbar ist und/oder als ein Planetenrollengewindetrieb ausgeführt ist.
- Formschließeinheit nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass das Lagerelement (16) als ein gesondertes Element ausgebildet ist und nicht in das Abstützelement (54) integriert ist.
- Formschließeinheit nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass das Abstützelement (54) zusätzliche radiale Abstützmittel (62) aufweist.
- Formschließeinheit nach einem der Ansprüche 2 bis 12, dadurch gekennzeichnet, dass die Spindelmutter (14) und/oder der Lagerraum (26) wenigstens eine Kühlwendel (36) aufweist.
- Formschließeinheit nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass ein vom Schmier- und/oder Kühlmedium gekühlter Lagerraum (26) vorgesehen ist, in dem ein Schmiermittel für die zusammenwirkenden Teile der Spindeleinheit (10) aufgenommen ist.
- Formschließeinheit nach Anspruch 14, dadurch gekennzeichnet, dass das Schmiermittel durch eine beim Zusammenspiel der Teile der Spindeleinheit erfolgende Bewegung der Lagereinheit (30) im Lagerraum (26) umwälzbar ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102016119581.2A DE102016119581A1 (de) | 2016-10-13 | 2016-10-13 | Formschließeinheit mit Wärmemanagement |
| PCT/EP2017/076248 WO2018069529A1 (de) | 2016-10-13 | 2017-10-13 | FORMSCHLIEßEINHEIT MIT WÄRMEMANAGEMENT |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3526481A1 EP3526481A1 (de) | 2019-08-21 |
| EP3526481B1 true EP3526481B1 (de) | 2020-08-26 |
Family
ID=60083338
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP17783867.9A Active EP3526481B1 (de) | 2016-10-13 | 2017-10-13 | Formschliesseinheit mit wärmemanagement |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US10933570B2 (de) |
| EP (1) | EP3526481B1 (de) |
| JP (1) | JP7041138B2 (de) |
| KR (1) | KR102338557B1 (de) |
| CN (1) | CN109804170B (de) |
| DE (1) | DE102016119581A1 (de) |
| WO (1) | WO2018069529A1 (de) |
Family Cites Families (29)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4290701A (en) * | 1979-07-06 | 1981-09-22 | Husky Injection Molding Systems Inc. | Injection-molding machine with reciprocating plasticizing screw |
| US5113670A (en) * | 1990-08-03 | 1992-05-19 | United Technologies Corporation | Bearing cooling arrangement for air cycle machine |
| US5585126A (en) * | 1992-08-25 | 1996-12-17 | Battenfeld Kunststoffmaschinen Ges.M.B.H. | Closing unit for form tools of an injection molding machine |
| DE19542453C2 (de) * | 1995-11-14 | 1998-05-20 | Karl Hehl | Vorrichtung zur Umwandlung einer Drehbewegung in eine Axialbewegung |
| JP3380750B2 (ja) * | 1998-08-25 | 2003-02-24 | 株式会社ソディック | 射出成形機の型締装置 |
| DE10060087C5 (de) * | 2000-12-02 | 2005-11-17 | Battenfeld Gmbh | Einspritzaggregat für eine Spritzgießmaschine |
| US6865963B2 (en) * | 2001-05-16 | 2005-03-15 | Sumitomo Heavy Industries, Ltd. | Apparatus and method for lubricating feed mechanism of forming machine |
| DE10202374A1 (de) * | 2002-01-23 | 2003-07-24 | Krauss Maffei Kunststofftech | Zweiplatten-Schließsystem einer Spritzgießmaschine |
| JP2004007952A (ja) * | 2002-03-29 | 2004-01-08 | Toshiba Mach Co Ltd | リニアモータと、リニアモータを用いた電動射出成形機 |
| TWI230653B (en) * | 2003-01-27 | 2005-04-11 | Sumitomo Heavy Industries | Molding machine with lubrication mechanism and method for lubricating molding machine |
| JP4473160B2 (ja) * | 2005-03-08 | 2010-06-02 | 東洋機械金属株式会社 | 成形機 |
| DE102006024712A1 (de) * | 2006-05-26 | 2007-12-06 | Siemens Ag | Antriebssystem |
| JP4957393B2 (ja) | 2007-06-04 | 2012-06-20 | 日本精工株式会社 | ボールねじ駆動装置 |
| US7942635B1 (en) * | 2007-08-02 | 2011-05-17 | Florida Turbine Technologies, Inc. | Twin spool rotor assembly for a small gas turbine engine |
| DE102008051285B3 (de) * | 2008-10-10 | 2010-07-22 | Karl Hehl | Formschließeinheit für Spritzgießformen |
| CN201428747Y (zh) * | 2009-06-30 | 2010-03-24 | 镇江市宏业科技有限公司 | 铝箔轧机支承辊轴承座冷却装置 |
| CN201471697U (zh) * | 2009-08-05 | 2010-05-19 | 王伟杰 | 单盲孔道的水冷回路装置 |
| AT509188B1 (de) * | 2009-11-23 | 2012-12-15 | Engel Austria Gmbh | Spindeltrieb mit schmierölablauf im dichtbereich |
| JP4824824B2 (ja) * | 2009-12-25 | 2011-11-30 | ファナック株式会社 | 射出成形機の自動給脂装置 |
| US8807970B2 (en) * | 2010-02-26 | 2014-08-19 | Flowserve Management Company | Cooling system for a multistage electric motor |
| DE102010048560B3 (de) | 2010-10-18 | 2012-03-15 | Arburg Gmbh + Co Kg | Spritzgießmaschine mit wenigstens zwei Kniehebelmechanismen |
| JP5598389B2 (ja) * | 2011-03-17 | 2014-10-01 | 株式会社豊田自動織機 | ターボチャージャの軸受ハウジングの冷却構造 |
| CN202273883U (zh) * | 2011-09-06 | 2012-06-13 | 阜新北鑫星液压有限公司 | 工程机械全液压自动风冷系统 |
| AT12643U1 (de) * | 2011-09-23 | 2012-09-15 | Engel Austria Gmbh | Spindelantrieb für eine spritzgiessmaschine |
| DE102012108061A1 (de) * | 2012-08-30 | 2014-03-06 | Mht Mold & Hotrunner Technology Ag | Vorformling |
| CN103978650B (zh) * | 2013-02-13 | 2017-07-18 | 住友重机械工业株式会社 | 注射成型机 |
| JP6005556B2 (ja) * | 2013-03-07 | 2016-10-12 | 住友重機械工業株式会社 | 射出成形機 |
| CN104235193A (zh) * | 2013-06-17 | 2014-12-24 | 何君 | 高速电动旋转机械用滚-滚动复合轴承系统及该旋转机械 |
| WO2015146569A1 (ja) * | 2014-03-22 | 2015-10-01 | Ntn株式会社 | 軸受装置の冷却構造 |
-
2016
- 2016-10-13 DE DE102016119581.2A patent/DE102016119581A1/de not_active Withdrawn
-
2017
- 2017-10-13 EP EP17783867.9A patent/EP3526481B1/de active Active
- 2017-10-13 CN CN201780061993.5A patent/CN109804170B/zh active Active
- 2017-10-13 WO PCT/EP2017/076248 patent/WO2018069529A1/de not_active Ceased
- 2017-10-13 KR KR1020197010658A patent/KR102338557B1/ko active Active
- 2017-10-13 JP JP2019520005A patent/JP7041138B2/ja active Active
- 2017-10-13 US US16/341,256 patent/US10933570B2/en active Active
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| KR20190071700A (ko) | 2019-06-24 |
| EP3526481A1 (de) | 2019-08-21 |
| CA3040044A1 (en) | 2018-04-19 |
| WO2018069529A1 (de) | 2018-04-19 |
| JP2019531940A (ja) | 2019-11-07 |
| US10933570B2 (en) | 2021-03-02 |
| US20200039134A1 (en) | 2020-02-06 |
| CN109804170B (zh) | 2020-10-27 |
| DE102016119581A1 (de) | 2018-04-19 |
| CN109804170A (zh) | 2019-05-24 |
| KR102338557B1 (ko) | 2021-12-13 |
| JP7041138B2 (ja) | 2022-03-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2726267B1 (de) | Drehvorrichtung für eine spritzgiessvorrichtung | |
| EP2349674B1 (de) | Elektrisch angetriebene formschliesseinheit an einer spritzgiessmaschine | |
| DE102013105435B3 (de) | Gießventil mit einem Nachverdichtungskolben | |
| EP3131728B1 (de) | Spritzgiessvorrichtung | |
| DE2166733A1 (de) | Spritz- blas-formwerkzeug fuer eine kunststoff-spritzgussmaschine | |
| EP2625019B1 (de) | Spritzgiessmaschine | |
| DE102012021836B4 (de) | Heißstempelnietvorrichtung | |
| EP2804737B1 (de) | Hydraulikeinrichtung mit einer temperiereinrichtung | |
| EP1075919A2 (de) | Verfahren und Vorrichtung zum Schliessen und Öffnen des Werkzeugs einer Kunststoffverarbeitungsmaschine | |
| AT516167A4 (de) | Temperiervorrichtung zum variothermen oder konventionellen Temperieren von Formwerkzeugen | |
| DE102023136107A1 (de) | Elektrische Maschine, insbesondere Elektromotor | |
| EP2825361B1 (de) | Spritzgiesswerkzeugplatte sowie spritzgiesswerkzeug mit einer solchen | |
| DE102004022306A1 (de) | Formkern | |
| DE102006021228A1 (de) | Zweiteiliger Bodeneinsatz | |
| AT525769A1 (de) | Schließeinheit für eine Formgebungsmaschine | |
| WO2018069529A1 (de) | FORMSCHLIEßEINHEIT MIT WÄRMEMANAGEMENT | |
| EP2015917A1 (de) | Bodeneinsatz mit wärmeisolation | |
| DE10022288C2 (de) | Vorrichtung zum Herstellen eines zum temperierenden Werkstücks | |
| DE102024123445B3 (de) | Spritzgießmaschine, Silikon-Spritzgießadapter und Verfahren zum Spritzgießen von Silikonwerkstücken | |
| DE102024121787B3 (de) | Antrieb für eine Formschließeinheit einer Spritzgießmaschine sowie Formschließeinheit oder Spritzgießmaschine mit solchem Antrieb | |
| EP1017522B1 (de) | Werkzeug insbesondere zum herstellen von kernen | |
| DE102021130503B4 (de) | Motoranordnung für eine Formgebungsvorrichtung, Motor für eine Formgebungsvorrichtung, Haltekörper, Formgebungsvorrichtung, Verwendungen eines Motors und eines Haltekörpers sowie Verfahren zur Kühlung eines Motors | |
| AT526153B1 (de) | Antriebseinheit für eine Formgebungsmaschine | |
| DE2215289A1 (de) | Verfahren und vorrichtung zur herstellung flaschenfoermiger kunststoffbehaelter durch blasverformung | |
| DE102012216715A1 (de) | Formwerkzeug und Verfahren zum Herstellen eines Kunststoffteils |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: UNKNOWN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20190503 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: F16C 19/54 20060101ALI20200227BHEP Ipc: F16C 37/00 20060101AFI20200227BHEP Ipc: B29C 45/17 20060101ALI20200227BHEP Ipc: B29C 45/84 20060101ALI20200227BHEP Ipc: B29C 45/83 20060101ALI20200227BHEP Ipc: B29C 45/66 20060101ALI20200227BHEP Ipc: B29C 45/72 20060101ALI20200227BHEP Ipc: F16C 19/38 20060101ALI20200227BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20200320 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502017006966 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1306661 Country of ref document: AT Kind code of ref document: T Effective date: 20200915 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: MERVELIX SARL, CH |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201228 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201127 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201126 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201126 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201226 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502017006966 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201013 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20201031 |
|
| 26N | No opposition filed |
Effective date: 20210527 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201013 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20211013 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200826 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211013 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230518 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: U11 Free format text: ST27 STATUS EVENT CODE: U-0-0-U10-U11 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20251101 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20251023 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250911 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20251021 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20251031 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20251027 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20251101 Year of fee payment: 9 |