EP3253565B1 - Pulverpresse mit kegeligem unterstempel, verfahren zum betrieb einer pulverpresse, pressling hergestellt mit einer pulverpresse, unterstempel einer pulverpresse und computerprogrammprodukt zum verfahren von unterstempeln einer presse - Google Patents
Pulverpresse mit kegeligem unterstempel, verfahren zum betrieb einer pulverpresse, pressling hergestellt mit einer pulverpresse, unterstempel einer pulverpresse und computerprogrammprodukt zum verfahren von unterstempeln einer presse Download PDFInfo
- Publication number
- EP3253565B1 EP3253565B1 EP16702397.7A EP16702397A EP3253565B1 EP 3253565 B1 EP3253565 B1 EP 3253565B1 EP 16702397 A EP16702397 A EP 16702397A EP 3253565 B1 EP3253565 B1 EP 3253565B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- powder press
- punch
- press
- powder
- lower punches
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B11/00—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses
- B30B11/02—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses using a ram exerting pressure on the material in a moulding space
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/02—Compacting only
- B22F3/03—Press-moulding apparatus therefor
- B22F2003/033—Press-moulding apparatus therefor with multiple punches working in the same direction
Definitions
- the present invention relates to a powder press with conical lower punches as well as a manufacturing method and a compact produced with the proposed powder press.
- a press structure is crucial for the possibility of what kind of parts can be pressed and how and in what time. From the DE 10 2014 003 726 The applicant produces a press for producing dimensionally stable green bodies in which the tool structures used have a shape optimization for elasticity compensation between individual tool levels. This requires a certain amount of technical effort in the design and manufacture of the tools.
- EP 1 764 173 A2 discloses a powder press according to the preamble of claim 1 with multi-part stamps, some of which are conical.
- US 2013/313741 A1 discloses a powder press with conically shaped punch holders.
- US 2,556,951A is aimed at a powder press with stamps.
- the object of the present invention is to create a simplified press structure that can be achieved in production using conventional methods and shortens tool changes and set-up time.
- a powder press is proposed with a tool structure which has nested lower punches, each lower punch having a cylindrical longitudinal extension which is guided through a die, with each longitudinal extension being followed by a conical widening. It is envisaged that a respective cone angle of the lower punch increases from the inside to the outside, while the respective longitudinal extent of the lower punch decreases from the inside to the outside.
- Each lower stamp is made in one piece.
- a further development provides that a stamp holder is directly connected to the conical widening.
- the conical widening of the respective lower punch widens to such an extent that an associated punch holder is flush with the lower punch on the outside.
- One embodiment for example, provides that the conical widening of the lower punch merges into a cylindrical section, the cylindrical section having fastening means for a punch holder.
- a punch holder is connected directly to a lower punch using a bayonet lock.
- a connection between the stamp holder and the lower stamp takes place without a pressure plate and a clamping plate.
- the tool assemblies can be made in one piece or in several parts using connection technology, possibly consisting of a head piece, connecting element and foot piece.
- the lower punches are constructed rotationally symmetrically.
- a powder press in which an upper punch has a longitudinal extension, in particular a cylindrical longitudinal extension, which extends into the die, with the longitudinal extension an extension follows.
- a plurality of nested upper punches is constructed in the same way as the lower punches described above and below.
- the upper punch and/or the lower punch are made in one piece.
- the upper punch and/or the lower punch is made in several parts.
- a compact made of metal powder is preferably produced using the method or the powder press.
- a compact is proposed, produced with a powder press as described above or below, with a density being constant along a cross section of the compact.
- a lower punch of a powder press is proposed, wherein the lower punch is produced by means of a machining process, by means of a primary forming process, pressing, cold forming and/or casting.
- a computer program product for moving the lower punches of a press is also proposed, with computer program code means being stored in a control system for execution, which enable a position-controlled movement of the lower punches.
- Fig. 1 shows a powder press, as is known from the prior art. This has a tool with a die, upper and lower punch as well as mandrels. Clamping plates, printing plates and stamp holders are used as accessories. On the one hand, the structure of the stamp shows the necessary size that must be provided for such a powder press. On the other hand, setting up requires a certain amount of effort, as the clamping plates and pressure plates have to be installed.
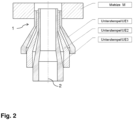
- Fig. 2 shows an exemplary, schematic tool structure with a conical substructure.
- the lower punches have an upper area, the punch head 1, which is preferably cylindrical and extends into the die.
- Each lower punch then has a conical extension, which is followed by a cylindrical section.
- the respective cone angle ie the angle that is enclosed by the angle of the cone shape to the vertically drawn axis 2, is preferably smaller from the outside to the inside or, to put it another way: a respective cone angle of the lower punch increases from the inside to the outside.
- the respective upper area becomes smaller from the inside out.
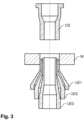
- Fig. 3 shows a proposed tool structure for conical lower punches, here consisting of die M, three lower punches UE1, UE2, UE3 and upper punch OS. While the three lower stamps are analogous to those from Fig. 2 are constructed, the upper punch OS can have a geometry that is the opposite but comparable to the lower punches.
- Fig. 4 shows a tool structure for conical lower punches, having a die and three lower punches, which are connected to the punch holders SH1, SH2, SH3 by a fastening means, here in the form of a bayonet lock 3.1, 3.2, 3.3.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Powder Metallurgy (AREA)
Description
- Die vorliegende Erfindung betrifft eine Pulverpresse mit kegeligen Unterstempeln sowie ein Herstellungsverfahren und einen Pressling, hergestellt mit der vorgeschlagenen Pulverpresse.
- Ein Pressenaufbau ist entscheidend für die Möglichkeit, was für Teile in welcher Zeit wie gepresst werden können. Aus der
DE 10 2014 003 726 der Anmelderin geht eine Presse zum Herstellen maßhaltiger Grünlinge hervor, bei der die verwendeten Werkzeugaufbauten eine Gestaltoptimierung zum Elastizitätsausgleich zwischen einzelnen Werkzeugebenen aufweisen. Hierfür ist ein gewisser technischer Aufwand bei der Auslegung wie auch bei der Herstellung der Werkzeuge notwendig. -
EP 1 764 173 A2 offenbart eine Pulverpresse gemäss dem Oberbegriff des Anspruchs 1 mit mehrteiligen Stempeln, die teilweise konisch ausgeführt sind. -
US 2013/313741 A1 offenbart eine Pulverpresse mit konisch geformten Stempelhaltern. -
US 2,556,951 A ist auf eine Pulverpresse mit Stempeln gerichtet. - Aufgabe der vorliegenden Erfindung ist es, einen vereinfachten Pressenaufbau zu schaffen, der in der Herstellung mit herkömmlichen Methoden erzielbar ist und einen Werkzeugwechsel nebst Zeit beim Einrichten verkürzt.
- Diese Aufgabe wird mit einer Pulverpresse mit den Merkmalen des Anspruchs 1, mit einem Verfahren mit den Merkmalen des Anspruchs 12 und mit einem Computerprogrammprodukt mit den Merkmalen des Anspruchs 14 gelöst. Vorteilhafte Weiterbildungen und Ausgestaltungen gehen aus den jeweiligen Unteransprüchen hervor, wobei ein oder mehrere Merkmale aus der Beschreibung wie auch aus den Figuren zu weiteren Ausgestaltungen kombiniert werden können. Die Formulierung der unabhängigen Ansprüche ist darüber hinaus als ein erster Versuch zu verstehen, den Gegenstand der Erfindung wiederzugeben. Daher können ein oder mehrere Merkmale der unabhängigen Ansprüche mit ein oder mehreren Merkmalen ergänzt, ausgetauscht oder auch gestrichen werden, um den Erfindungsgegenstand näher zu fassen.
- Es wird eine Pulverpresse mit einem Werkzeugaufbau vorgeschlagen, der ineinander geschachtelte Unterstempel hat, wobei jeder Unterstempel eine zylindrische Längserstreckung aufweist, die durch eine Matrize geführt wird, wobei sich an jede Längserstreckung eine kegelförmige Verbreiterung anschließt. Es ist vorgesehen, dass ein jeweiliger Kegelwinkel der Unterstempel von innen nach außen zunimmt, während die jeweilige Längserstreckung der Unterstempel von innen nach außen abnimmt. Jeder Unterstempel ist einstückig ausgeführt.
- Eine Weiterbildung sieht vor, dass an die kegelförmige Verbreiterung ein Stempelhalter direkt anschließt.
- Bevorzugt ist es, dass die kegelförmige Verbreiterung des jeweiligen Unterstempels sich soweit verbreitert, dass ein zugehöriger Stempelhalter seitlich außen bündig mit dem Unterstempel abschließt.
- Eine Ausgestaltung sieht zum Beispiel vor, dass die kegelförmige Verbreiterung des Unterstempels in einen zylindrischen Abschnitt übergeht, wobei der zylindrische Abschnitt Befestigungsmittel für einen Stempelhalter aufweist.
- Weiterhin ist es bevorzugt, dass ein Stempelhalter direkt mit einem Unterstempel mittels eines Bajonettverschlusses verbunden ist.
- Gemäß einer bevorzugten Ausgestaltung ist vorgesehen, dass eine Verbindung zwischen Stempelhalter und Unterstempel ohne Druckplatte und Klemmplatte erfolgt.
- Dieses ermöglicht ebenfalls einen vereinfachten Werkzeugaufbau bei gleichzeitigem Verzicht auf das übliche Zubehör, insbesondere Druckplatten, mit dem Ziel der:
- Kraftfußoptimierung durch geometrisch einfache, trichterförmige Werkzeuggestaltung, besonders bei rotationssymmetrischen Werkzeugen einsetzbar;
- Reduzierter Aufwand in der Konstruktion durch Verzicht auf die Gestaltoptimierung;
- Verzicht auf additive Herstellverfahren, da die einfachen Werkzeugelemente in der Regel auf Standard-Werkzeugmaschinen durch spanabhebende Verfahren hergestellt werden können;
- Verkürzung der inneren Werkzeugelemente, auch unter Inkaufnahme der Verlängerung der äußeren Werkzeugelemente;
- Verzicht auf einen vollkommenen Elastizitätsausgleich: der Ausgleich wird in der Regel nach wie vor durch die Positionsregelung der Maschine vorgenommen.
- Die Werkzeugaufbauten können sowohl einstückig, als auch durch Verbindungstechnik mehrteilig aus ggf. Kopfstück, Verbindungselement und Fußstück bestehen.
- Insbesondere unter dem Aspekt einer gleichmäßigen Druckaufprägung, wie vor allem auch Druckentlastung über eine Breite des Presslings, ist es vorteilhaft, dass die Unterstempel rotationssymmetrisch aufgebaut sind.
- Gemäß einem weiteren Gedanken der Erfindung, der unabhängig wie auch abhängig von dem obigen Gegenstand beansprucht werden kann, ist eine Pulverpresse vorgesehen, bei der ein Oberstempel eine Längserstreckung, insbesondere eine zylindrische Längserstreckung aufweist, die sich in die Matrize erstreckt, wobei sich an die Längserstreckung eine Erweiterung anschließt. Bevorzugt ist eine Mehrzahl an ineinander verschachtelten Oberstempeln so aufgebaut wie die oben bzw. nachfolgend beschriebenen Unterstempel.
- Weiterhin ist es bevorzugt, wenn der Oberstempel und/oder der Unterstempel einstückig hergestellt sind. Auch besteht die Möglichkeit, dass der Oberstempel und/oder der Unterstempel mehrteilig hergestellt ist.
- Gemäß einem weiteren Gedanken der Erfindung, der unabhängig wie auch abhängig von dem obigen Vorschlag einer Pulverpresse verfolgt werden kann, wird ein Verfahren zum Betrieb einer Pulverpresse mit Unterstempeln wie oben und nachfolgend beschrieben, wobei ein Ausgleich beim Verfahren der Unterstempel über eine Positionsregelung erfolgt.
- Bevorzugt wird mit dem Verfahren bzw. der Pulverpresse ein Pressling aus Metallpulver erzeugt.
- Weiterhin wird ein Pressling vorgeschlagen, hergestellt mit einer Pulverpresse wie oben bzw. nachfolgend beschrieben, wobei eine Dichte entlang eines Querschnitts des Presslings gleichbleibend ist.
- Weiterhin wird ein Unterstempel einer Pulverpresse vorgeschlagen, wobei der Unterstempel mittels eines spanabhebenden Verfahrens, mittels eines Urformverfahrens, eines Pressens, eines Kaltumformens und/oder eines Gießens hergestellt ist.
- Auch wird ein Computerprogrammprodukt zum Verfahren von Unterstempeln einer Presse vorgeschlagen, wobei Computerprogrammcodemittel zum Ablauf in einer Steuerung hinterlegt sind, die ein positionsgeregeltes Verfahren der Unterstempel ermöglichen.
- Weitere vorteilhafte Merkmale und Ausgestaltungen gehen aus den nachfolgenden Figuren hervor. Ein oder mehrere Merkmale aus ein oder mehreren Figuren wie auch aus der obigen Beschreibung können dabei zusammen zu weiteren Ausgestaltungen verbunden werden. Insbesondere dienen die Figuren der Erläuterung der Erfindung und sollen diese jedoch nicht beschränken. Es zeigen:
- Fig. 1:
- Eine Pulverpresse aus dem Stand der Technik,
- Fig. 2:
- Einen beispielhaften, schematischen Werkzeugaufbau mit kegeligen Unterstempeln,
- Fig. 3:
- Eine Erweiterung der Darstellung aus
Fig. 2 um einen entsprechend angepassten Oberstempel, und - Fig. 4:
- Eine schematische Ansicht des Werkzeugaufbaus mit kegeligen Unterstempel und angebrachtem Stempelhalter.
-
Fig. 1 zeigt eine Pulverpresse, wie sie aus dem Stand der Technik bekannt ist. Diese weist ein Werkzeug mit Matrize, Ober- und Unterstempel wie auch Dorne auf. Als Zubehör werden Klemmplatten, Druckplatten und Stempelhalter eingesetzt. Der Aufbau der Stempel zeigt zum einen die notwendige Größe, die für eine derartige Pulverpresse vorgesehen sein muss. Zum anderen erfordert das Einrichten einen gewissen Aufwand, da hierfür die Klemmplatten und Druckplatten mit eingebaut werden müssen. -
Fig. 2 zeigt einen beispielhaften, schematischen Werkzeugaufbau mit einem kegeligen Unterbau. Vorgesehen sind bei dieser Ausführung neben der Matrize M drei Unterstempel UE1, UE2, UE3. Die Unterstempel haben einen oberen Bereich, den Stempelkopf 1, der vorzugsweise zylindrisch ist und sich in die Matrize erstreckt. Jeder Unterstempel hat sodann eine kegelförmige Erweiterung, an die sich hier jeweils ein zylindrischer Abschnitt anschließt. Der jeweilige Kegelwinkel, d. h. der Winkel, der durch den Winkel der Kegelform zur senkrecht eingezeichneten Achse 2 eingeschlossen ist, wird vorzugsweise von außen nach innen kleiner oder anders ausgedrückt: Ein jeweiliger Kegelwinkel der Unterstempel nimmt von innen nach außen zu. Der jeweilige obere Bereich ist hingegen von innen nach au-βen kleiner werdend. -
Fig. 3 zeigt einen vorgeschlagenen Werkzeugaufbau für kegelige Unterstempel, hier bestehend aus Matrize M, drei Unterstempeln UE1, UE2, UE3 und Oberstempel OS. Während die drei Unterstempel analog zu denjenigen ausFig. 2 aufgebaut sind, kann der Oberstempel OS eine zu den Unterstempeln umgekehrte, aber vergleichbare Geometrie aufweisen. -
Fig. 4 zeigt einen Werkzeugaufbau für kegelige Unterstempel, aufweisend eine Matrize und drei Unterstempel, die durch ein Befestigungsmittel, hier in Form eines Bajonettverschlusses 3.1, 3.2, 3.3, mit den Stempelhaltern SH1, SH2, SH3 verbunden sind.
Claims (14)
- Pulverpresse mit einem Werkzeugaufbau, der einen kegeligen Unterstempel (UE1, UE2, UE3) mit ineinander geschachtelten Unterstempeln (UE1, UE2, UE3) hat, wobei jeder Unterstempel (UE1, UE2, UE3) eine zylindrische Längserstreckung aufweist, die durch eine Matrize (M) geführt wird, wobei sich an jede Längserstreckung eine kegelförmige Verbreiterung anschließt, wobei ein jeweiliger Kegelwinkel der Unterstempel (UE1, UE2, UE3) von innen nach außen zunimmt; dadurch gekennzeichnet, dass jeder Unterstempel (UE1, UE2, UE3) einstückig hergestellt ist.
- Pulverpresse nach Anspruch 1, dadurch gekennzeichnet, dass die jeweilige Längserstreckung der Unterstempel (UE1, UE2, UE3) von innen nach außen abnimmt.
- Pulverpresse nach Anspruch 1, dadurch gekennzeichnet, dass an die kegelförmige Verbreiterung ein Stempelhalter (SH1, SH2, SH3) direkt anschließt.
- Pulverpresse nach Anspruch 1, 2 oder 3, dadurch gekennzeichnet, dass die kegelförmige Verbreiterung des jeweiligen Unterstempels (UE1, UE2, UE3) sich soweit verbreitert, dass ein zugehöriger Stempelhalter (SH1, SH2, SH3) seitlich außen bündig mit dem Unterstempel (UE1, UE2, UE3) abschließt.
- Pulverpresse nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die kegelförmige Verbreiterung des Unterstempels (UE1, UE2, UE3) in einen zylindrischen Abschnitt übergeht, wobei der zylindrische Abschnitt Befestigungsmittel für einen Stempelhalter (SH1, SH2, SH3) aufweist.
- Pulverpresse nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass ein Stempelhalter (SH1, SH2, SH3) direkt mit einem Unterstempel (UE1, UE2, UE3) mittels eines Bajonettverschlusses (3.1, 3.2, 3.3) verbunden ist.
- Pulverpresse nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass eine Verbindung zwischen Stempelhalter (SH1, SH2, SH3) und Unterstempel (UE1, UE2, UE3) ohne Druckplatte und Klemmplatte erfolgt.
- Pulverpresse nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Unterstempel (UE1, UE2, UE3) rotationssymmetrisch aufgebaut sind.
- Pulverpresse nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass ein Oberstempel (OS) eine Längserstreckung, insbesondere eine zylindrische Längserstreckung aufweist, die sich in die Matrize (M) erstreckt, wobei sich an die Längserstreckung eine Erweiterung anschließt.
- Pulverpresse nach Anspruch 9, dadurch gekennzeichnet, dass der Oberstempel (OS) einstückig hergestellt ist.
- Pulverpresse nach einem der vorhergehenden Ansprüche 9 und 10, dadurch gekennzeichnet, dass der Oberstempel (OS) mehrteilig hergestellt ist.
- Verfahren zum Betrieb einer Pulverpresse mit Unterstempeln (UE1, UE2, UE3) nach einem der Ansprüche 1 bis 10, wobei ein Ausgleich beim Verfahren der Unterstempel (UE1, UE2, UE3) über eine Positionsregelung erfolgt.
- Verfahren nach Anspruch 12, dadurch gekennzeichnet, dass ein Pressling aus Metallpulver erzeugt wird.
- Computerprogrammprodukt zum Verfahren von Unterstempeln (UE1, UE2, UE3) einer Presse nach einem der Ansprüche 1-11, wobei Computerprogrammcodemittel zum Ablauf in einer Steuerung hinterlegt sind, die ein positionsgeregeltes Verfahren der Unterstempel (UE1, UE2, UE3) ermöglichen.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102015201785.0A DE102015201785A1 (de) | 2015-02-02 | 2015-02-02 | Pulverpresse mit kegeligem Unterstempel |
| PCT/EP2016/051932 WO2016124497A1 (de) | 2015-02-02 | 2016-01-29 | Pulverpresse mit kegeligem unterstempel, verfahren zum betrieb einer pulverpresse, pressling hergestellt mit einer pulverpresse, unterstempel einer pulverpresse und computerprogrammprodukt zum verfahren von unterstempeln einer presse |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3253565A1 EP3253565A1 (de) | 2017-12-13 |
| EP3253565B1 true EP3253565B1 (de) | 2024-03-20 |
Family
ID=55273259
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP16702397.7A Active EP3253565B1 (de) | 2015-02-02 | 2016-01-29 | Pulverpresse mit kegeligem unterstempel, verfahren zum betrieb einer pulverpresse, pressling hergestellt mit einer pulverpresse, unterstempel einer pulverpresse und computerprogrammprodukt zum verfahren von unterstempeln einer presse |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20180022050A1 (de) |
| EP (1) | EP3253565B1 (de) |
| CN (1) | CN107427916B (de) |
| DE (1) | DE102015201785A1 (de) |
| ES (1) | ES2980789T3 (de) |
| WO (1) | WO2016124497A1 (de) |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102014003726A1 (de) * | 2014-03-18 | 2015-09-24 | Gkn Sinter Metals Engineering Gmbh | Presse zum Herstellen maßhaltiger Grünlinge und Verfahren zum Herstellen |
| DE102015201966A1 (de) | 2015-02-04 | 2016-08-04 | Gkn Sinter Metals Engineering Gmbh | Pulverpresse mit kegeligem Unterbau |
| DE102015012004A1 (de) | 2015-09-18 | 2017-03-23 | Gkn Sinter Metals Engineering Gmbh | Sinterpresse mit axial kontrollierter Verformung und Verfahren hierzu |
| DE102015012005A1 (de) | 2015-09-18 | 2017-03-23 | Gkn Sinter Metals Engineering Gmbh | Stempelwerkzeug einer Sinterpresse und Verfahren hierzu |
| CN110621503B (zh) | 2017-02-08 | 2022-09-16 | Gkn烧结金属工程有限公司 | 具有偏移补偿的工具组 |
| DE102018107637A1 (de) | 2018-03-29 | 2019-10-02 | Dorst Technologies Gmbh & Co. Kg | Kalibrierverfahren |
| EP3900923B1 (de) * | 2020-04-22 | 2023-11-01 | PrivMed X AB | Verfahren zum automatisierten herstellen von individualisierten tabletten und tablettenpresse zur automaitisierten herstellung von individualisierten tabletten |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015201966A1 (de) * | 2015-02-04 | 2016-08-04 | Gkn Sinter Metals Engineering Gmbh | Pulverpresse mit kegeligem Unterbau |
| DE102015012004A1 (de) * | 2015-09-18 | 2017-03-23 | Gkn Sinter Metals Engineering Gmbh | Sinterpresse mit axial kontrollierter Verformung und Verfahren hierzu |
| DE102015012005A1 (de) * | 2015-09-18 | 2017-03-23 | Gkn Sinter Metals Engineering Gmbh | Stempelwerkzeug einer Sinterpresse und Verfahren hierzu |
Family Cites Families (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2556951A (en) * | 1944-06-05 | 1951-06-12 | Stokes Machine Co | Powdered material compacting press |
| US4153399A (en) * | 1977-09-08 | 1979-05-08 | Ptx-Pentronix, Inc. | Multiple punch tool set for powder compacting press |
| DE3241383C2 (de) * | 1982-11-09 | 1986-09-04 | Institut po Metalosnanie i Technologia na Metalite, Sofia/Sofija | Vorrichtung zum Umformen von Metall durch Fließpressen |
| GB2129724B (en) * | 1982-11-11 | 1986-01-29 | Inst Po Metalloznanie I Tekno | Extrusion and stamping of material |
| JPH05140609A (ja) * | 1991-02-08 | 1993-06-08 | Keita Hirai | 段付品汎用成型プレス |
| JPH0788699A (ja) * | 1993-09-24 | 1995-04-04 | Mitsubishi Materials Corp | 金型装置 |
| JP3158244B2 (ja) * | 1996-11-22 | 2001-04-23 | 三菱マテリアル株式会社 | 多段ヘリカルギアの製造方法及びその粉末成形用金型 |
| SE515822C2 (sv) * | 1999-12-30 | 2001-10-15 | Skf Nova Ab | Metod och anordning för kompaktering av pulvermetallkroppar |
| JP2004291046A (ja) * | 2003-03-27 | 2004-10-21 | Sumitomo Denko Shoketsu Gokin Kk | 粉末成形における成形体のクラック防止方法及び装置 |
| DE102005044759B4 (de) * | 2005-09-20 | 2007-07-12 | Sms Meer Gmbh | Vorrichtung zum Herstellen eines Formteils |
| DE102007010360A1 (de) * | 2007-03-03 | 2008-09-04 | Dorst Technologies Gmbh & Co. Kg | Pressstempel-Befestigungsvorrichtung und Verfahren zum Befestigen eines Stempels in einer Presse |
| DE102010051513A1 (de) * | 2010-11-16 | 2012-05-16 | Dorst Technologies Gmbh & Co. Kg | Keramikpulver- und/oder Metallpulver-Pressenwerkzeug, Keramikpulver- und/oder Metallpulver-Presse, modulares System mit einem solchen Pressenwerkzeug, Verfahren zum Zusammensetzen eines solchen Pressenwerkzeugs |
| DE102013006831B4 (de) * | 2013-04-22 | 2015-05-28 | Schuler Pressen Gmbh | Spannsystem zum Spannen eines Stempels an einem Stößel einer Fließdruckpresse |
| CN103331444B (zh) * | 2013-07-05 | 2015-09-30 | 益阳市新纪元粉末冶金有限公司 | 粉末冶金制品压制成型模具及应用和成型脱模方法 |
| CN203651029U (zh) * | 2013-12-24 | 2014-06-18 | 北京国药龙立自动化技术有限公司 | 单工位等密度压机 |
| DE102014003726A1 (de) | 2014-03-18 | 2015-09-24 | Gkn Sinter Metals Engineering Gmbh | Presse zum Herstellen maßhaltiger Grünlinge und Verfahren zum Herstellen |
-
2015
- 2015-02-02 DE DE102015201785.0A patent/DE102015201785A1/de not_active Withdrawn
-
2016
- 2016-01-29 WO PCT/EP2016/051932 patent/WO2016124497A1/de not_active Ceased
- 2016-01-29 CN CN201680008351.4A patent/CN107427916B/zh active Active
- 2016-01-29 EP EP16702397.7A patent/EP3253565B1/de active Active
- 2016-01-29 ES ES16702397T patent/ES2980789T3/es active Active
- 2016-01-29 US US15/547,708 patent/US20180022050A1/en not_active Abandoned
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015201966A1 (de) * | 2015-02-04 | 2016-08-04 | Gkn Sinter Metals Engineering Gmbh | Pulverpresse mit kegeligem Unterbau |
| DE102015012004A1 (de) * | 2015-09-18 | 2017-03-23 | Gkn Sinter Metals Engineering Gmbh | Sinterpresse mit axial kontrollierter Verformung und Verfahren hierzu |
| DE102015012005A1 (de) * | 2015-09-18 | 2017-03-23 | Gkn Sinter Metals Engineering Gmbh | Stempelwerkzeug einer Sinterpresse und Verfahren hierzu |
Also Published As
| Publication number | Publication date |
|---|---|
| WO2016124497A1 (de) | 2016-08-11 |
| CN107427916A (zh) | 2017-12-01 |
| CN107427916B (zh) | 2020-09-29 |
| DE102015201785A1 (de) | 2016-08-04 |
| US20180022050A1 (en) | 2018-01-25 |
| EP3253565A1 (de) | 2017-12-13 |
| ES2980789T3 (es) | 2024-10-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3253567B1 (de) | Pulverpresse mit kegeligem unterbau | |
| WO2016124497A1 (de) | Pulverpresse mit kegeligem unterstempel, verfahren zum betrieb einer pulverpresse, pressling hergestellt mit einer pulverpresse, unterstempel einer pulverpresse und computerprogrammprodukt zum verfahren von unterstempeln einer presse | |
| EP3253566B1 (de) | Gestaltoptimierte pm-werkzeugkomponenten unter verwendung von verbindungstechnologie | |
| EP2987566B1 (de) | Vorrichtung und Verfahren zum Kalibrieren von Grat aufweisenden Schnittflächen an Stanz- oder Feinschneidteilen | |
| DE2610568C3 (de) | Verfahren und Vorrichtung zur Herstellung von Kurbelhüben | |
| EP2484462B1 (de) | Verfahren zum Erzeugen einer Schmiedevorform und Umformvorrichtung oder Warmstauchvorrichtung | |
| DE102014003726A1 (de) | Presse zum Herstellen maßhaltiger Grünlinge und Verfahren zum Herstellen | |
| DE68914129T2 (de) | Matrize zum Strangpressen von Metallen. | |
| EP2982458B1 (de) | Anordnung zur verwendung beim herstellen einer teilbaren giessform | |
| EP3349925B1 (de) | Sinterpresse mit axial kontrollierter verformung und verfahren hierzu | |
| EP2877298B1 (de) | Direktes oder indirektes metallrohrstrangpressverfahren, metallrohrstrangpresse sowie stranggepresstes metallrohr | |
| EP3349926B1 (de) | Stempelwerkzeug einer sinterpresse und verfahren hierzu | |
| WO2018114502A1 (de) | Matrize für eine presse und verfahren zur herstellung eines grünlings mit einer presse | |
| WO2019002600A1 (de) | Ebenenplatte eines pressenwerkzeugs | |
| DE102014004521A1 (de) | Pressenvorrichtung zur Umformung eines Blechbauteils | |
| DE102017130680B4 (de) | Matrize für eine Presse sowie Verfahren zur Herstellung mindestens eines Grünlings mit einer solchen Presse | |
| EP3645261B1 (de) | Ebenenplatte eines pressenwerkzeugs | |
| DE102015122656A1 (de) | Verfahren zum auspressen von werkteilen vom typ hülse sowie vorrichtung zu dessen umsetzung | |
| EP3075504A1 (de) | Vorrichtung zur herstellung von betonformteilen in einer formmaschine | |
| DE10042896B4 (de) | Verfahren zum Herstellen eines Ringelements | |
| EP3645259B1 (de) | Ebenenplatte eines pressenwerkzeugs | |
| EP3645262B1 (de) | Ebenenplatte eines pressenwerkzeugs | |
| DE102019002187A1 (de) | Verfahren und Vorrichtung zum Herstellen eines Bauteils mit Gewinde | |
| DE202010013183U1 (de) | Presse zum Umformen zylindrischer Werkstücke | |
| EP3393694B1 (de) | Verfahren zur umformenden herstellung einer verzahnung und werkzeugvorrichtung zur kalibrierung des verzahnungseinlaufs und/oder verzahnungsauslaufs |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20170803 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17Q | First examination report despatched |
Effective date: 20210622 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230601 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20240103 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502016016425 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240621 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240620 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20240320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240620 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240620 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240621 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2980789 Country of ref document: ES Kind code of ref document: T3 Effective date: 20241003 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240720 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240722 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240722 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240720 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502016016425 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| 26N | No opposition filed |
Effective date: 20241223 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250129 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240320 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250131 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250131 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20250131 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 1667488 Country of ref document: AT Kind code of ref document: T Owner name: GKN POWER METALLURGY GMBH, DE Effective date: 20251103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250129 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20260217 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20260120 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20260119 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20260130 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20260121 Year of fee payment: 11 |