EP2734322B1 - GIEßKERN EINER GUSSFORM ZUR HERSTELLUNG EINES ZYLINDERS - Google Patents
GIEßKERN EINER GUSSFORM ZUR HERSTELLUNG EINES ZYLINDERS Download PDFInfo
- Publication number
- EP2734322B1 EP2734322B1 EP12731009.2A EP12731009A EP2734322B1 EP 2734322 B1 EP2734322 B1 EP 2734322B1 EP 12731009 A EP12731009 A EP 12731009A EP 2734322 B1 EP2734322 B1 EP 2734322B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- core
- casting
- cylinder
- sand
- steel
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 238000005266 casting Methods 0.000 title claims description 41
- 229910000831 Steel Inorganic materials 0.000 claims description 32
- 239000010959 steel Substances 0.000 claims description 32
- 238000002485 combustion reaction Methods 0.000 claims description 12
- 229910052751 metal Inorganic materials 0.000 claims description 6
- 239000002184 metal Substances 0.000 claims description 6
- 238000004519 manufacturing process Methods 0.000 claims description 4
- 229910052782 aluminium Inorganic materials 0.000 claims description 3
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 3
- 238000000034 method Methods 0.000 claims description 3
- 239000004411 aluminium Substances 0.000 claims 1
- 238000001816 cooling Methods 0.000 description 11
- 230000015572 biosynthetic process Effects 0.000 description 10
- 239000004576 sand Substances 0.000 description 7
- 230000017525 heat dissipation Effects 0.000 description 5
- 229910001018 Cast iron Inorganic materials 0.000 description 2
- 230000001419 dependent effect Effects 0.000 description 2
- 239000007787 solid Substances 0.000 description 2
- 238000007711 solidification Methods 0.000 description 2
- 230000008023 solidification Effects 0.000 description 2
- 229910001208 Crucible steel Inorganic materials 0.000 description 1
- 238000010521 absorption reaction Methods 0.000 description 1
- 230000002411 adverse Effects 0.000 description 1
- 238000005253 cladding Methods 0.000 description 1
- -1 for example Inorganic materials 0.000 description 1
- 238000000227 grinding Methods 0.000 description 1
- 238000002955 isolation Methods 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 230000001737 promoting effect Effects 0.000 description 1
- 238000007528 sand casting Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D15/00—Casting using a mould or core of which a part significant to the process is of high thermal conductivity, e.g. chill casting; Moulds or accessories specially adapted therefor
- B22D15/02—Casting using a mould or core of which a part significant to the process is of high thermal conductivity, e.g. chill casting; Moulds or accessories specially adapted therefor of cylinders, pistons, bearing shells or like thin-walled objects
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/10—Cores; Manufacture or installation of cores
- B22C9/103—Multipart cores
Definitions
- the present invention relates to a casting core for a casting mold for producing a cylinder of an internal combustion engine according to the preamble of claim 1.
- the invention also relates to a method for producing a cast cylinder.
- a generic casting core for casting cast iron cylinders of air cooled internal combustion engines.
- a core is provided from a compact metal cooling bush provided with bores, which is provided on all sides with a sand cladding.
- the JP 60 040663 A discloses a casting core of a casting mold for producing a cylinder of an internal combustion engine.
- the casting core comprises a radially outwardly projecting part and is formed in two parts.
- the US 4,252,175 discloses the formation of a two-part casting core with a sand core and a steel core.
- the JP 1 309774 A treats a two-part casting core of sand and a metal bush.
- the US 4,003,422 discloses a one-piece casting core which may be formed of sand.
- a socket is formed of metal and thus represents a steel core.
- the present invention is concerned with the problem of providing for a casting core of the generic type an improved or at least one alternative embodiment, which is characterized in particular by an improved thermal management.
- the present invention is based on the general idea of forming a casting core of a mold for producing a cylinder of an internal combustion engine, in particular for producing an aluminum cylinder of a two-stroke engine, not one piece of sand as before, but according to the invention of two parts, namely a sand core and a associated steel core.
- a sand core preferably only the upper part of G mankerns, that is, that region which is later assigned to a combustion chamber of the cylinder, formed of sand, whereas a lower region, that is, the region which is assigned to a later cylinder surface, is formed of steel.
- the steel core takes in comparison to the sand core significantly more heat and performs this comparatively, making it especially in the cylinder surface to a significantly increased temperature difference between the cylinder surface (surface) and further inside and thereby voids can be avoided or at least reduced , Since such voids are extremely critical, particularly in the area of the later cylinder running surfaces, the steel core is used in this area in particular in order to achieve as rapid / uniform cooling of the cast cylinder as possible, together with the outermost mold and also made of metal. Due to the core made of steel now as rapid cooling in the cylinder running surface inwards as outward to the steel mold, whereby the possibly forming voids are forced into the interior of the cylinder wall and indeed so deep that they no longer at a later processing be opened.
- the casting core is furthermore formed by a sand core, as a result of which, in particular, difficult casting geometries, in particular also undercuts, can be produced.
- the essential advantage of the casting core according to the invention is that the voids formation is at least greatly reduced or preferably completely avoided and even when voids appear they are arranged so deeply in the cylinder wall that they can be rotated or honed during a later processing step. can not be opened and thereby adversely affect the cylinder running properties.
- the sand core engages via a mandrel in a corresponding recess on the steel core.
- the sand core is preferably positively connected to the steel core, whereby the handling of the From the sand core and the steel core formed G thinkkerns is significantly simplified.
- the sand core and / or the steel core are each solid. Due to the massive formation of the sand core and / or the steel core, these are relatively robust and therefore ideally suited for use in modern foundries. At the same time allows a massive training, especially the steel core, and a significantly improved heat absorption and thus a significantly improved heat dissipation, whereby a uniform solidification or cooling of the cylinder can be achieved.
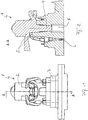
- An inventive casting core 1 of a casting mold not shown otherwise for the production of a likewise not shown cylinder of an internal combustion engine, in particular for producing a cylinder of a two-stroke engine, a sand core 2 and a steel core 3 connected thereto.
- the casting core 1 is formed in two parts, wherein the sand core 2 at least partially covers an area of a later combustion chamber of the cylinder, whereas the steel core 3 at least partially covers an area of a later cylinder running surface.
- the occurrence of blowholes is extremely critical, as this can negatively affect the piston running properties. It is therefore essential to avoid such voids.
- voids are formed in particular by the fact that the cast cylinder solidifies unevenly and with large temperature differences, which was especially the use of hitherto customary and made entirely of sand casting cores on the agenda.
- sand core 1 of the invention can provide a remedy by being formed in the region of a later cylinder surface of the steel core 3, thereby enabling a comparatively high heat dissipation.
- the high heat dissipation in particular in the region of the later cylinder running surface causes a small temperature difference of the cooling cylinder between the inner steel core 3 and the outer, not shown mold.
- the mold forms an outer shape of the casting mold, whereas the casting core 1 represents the inner shape of the casting mold.
- the steel core 3 urges the forming voids so deeply into the interior of the steel core 3 by a high cooling rate Cylinder wall, that they are not opened even in a later processing.
- the sand core 2 has a mandrel 4, which engages in a corresponding recess 5 on the steel core 3.
- a mandrel 4 on the steel core 3 and the corresponding formation of the recess 5 on the sand core 2 is conceivable.
- a positive connection between the sand core 2 and the steel core 3 can be achieved.
- / the sand core 2 and / or the steel core 3 are solid, which in particular in the region of the steel core 3, a high and a rapid heat dissipation can be done.
- Steel has a significantly improved thermal conductivity compared to sand.
- 3 openings 6 may be provided in the steel core, via which, for example, a vent or cooling can take place.
- the casting core 1 according to the invention is used for the production of cast cylinders and in this process is surrounded by a mold, not shown.
- the casting core constitutes the casting mold together with the mold.
- the material used for casting the cylinder may, for example, be cast steel but also light metal, such as, for example, aluminum.
- the casting core 1 With the casting core 1 according to the invention, a uniform cooling of the cast cylinder from inside and outside and, associated therewith, a significantly reduced voids formation in the region of the critical regions can be achieved, as a result of which the quality of the cylinders produced in this way can be significantly increased. If, contrary to expectations, cavities or inclusions nevertheless form, they are usually arranged so deeply in the cylinder that they are not exposed during a later processing step, for example when grinding, turning or honing, and are therefore harmless.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
Description
- Die vorliegende Erfindung betrifft einen Gießkern für eine Gussform zur Herstellung eines Zylinders einer Brennkraftmaschine gemäß dem Oberbegriff des Anspruchs 1. Die Erfindung betrifft außerdem ein Verfahren zur Herstellung eines gegossenen Zylinders.
- Aus der
DE 35 09 015 A1 ist ein gattungsgemäßer Gießkern zum Gießen von aus Grauguss bestehenden Zylindern von Luft gekühlten Verbrennungsmotoren bekannt. Um dabei insbesondere ein hinsichtlich einer unerwünschten Lunkerbildung ungünstiges Abkühlverhalten optimieren zu können, wird ein Kern vorgesehen aus einer mit Bohrungen versehenen kompakten Metallkühlbüchse, die allseitig mit einer Sandverkleidung versehen ist. Mit diesem Gießkern mit intensiver Wärmeabfuhr wird bei der Erstarrung der in der Gussform befindlichen Graugussschmelze eine gezielte Formierung einer Gasdichte perlitischer Struktur der Zylinderwand, besonders der Fläche der Zylinderbohrung und einer die Wärmeleitung fördernden grauen Struktur in den Kühlrippen ermöglicht, wodurch hohe Qualitätsansprüche an die damit hergestellten Zylinder erfüllt werden sollen. - Generell besteht bei bekannten Gießverfahren zum Herstellen von gegossenen Zylindern für Brennkraftmaschinen das Problem, dass bei Verwendung eines Sandkernes eine ungleichmäßige Abkühlung des gegossenen Zylinders stattfindet, wodurch hohe Temperaturdifferenzen innerhalb des Zylinders auftreten. Diese vergleichsweise hohen Temperaturdifferenzen können zu einer Lunkerbildung, insbesondere auf einer späteren Zylinderlaufbahn, führen, was unbedingt zu vermeiden ist.
- Die
JP 60 040663 A - Die
US 4,252,175 offenbart die Ausbildung eines zweiteiligen Gießkerns mit einem Sandkern und einem Stahlkern. - Die
JP 1 309774 A - Die
US 4,003,422 offenbart einen einteiligen Gießkern, der aus Sand ausgebildet sein kann. Eine Buchse ist aus Metall ausgebildet und stellt somit einen Stahlkern dar. - Die vorliegende Erfindung beschäftigt sich mit dem Problem, für einen Gießkern der gattungsgemäßen Art eine verbesserte oder zumindest eine alternative Ausführungsform anzugeben, die sich insbesondere durch ein verbessertes Wärmemanagement auszeichnet.
- Dieses Problem wird erfindungsgemäß durch die Gegenstände der unabhängigen Ansprüche gelöst. Vorteilhafte Ausführungsformen sind Gegenstand der abhängigen Ansprüche.
- Die vorliegende Erfindung beruht auf dem allgemeinen Gedanken, einen Gießkern einer Gussform zur Herstellung eines Zylinders einer Brennkraftmaschine, insbesondere zur Herstellung eines Aluminium-Zylinders eines Zweitaktmotors, nicht wie bisher einteilig aus Sand auszubilden, sondern erfindungsgemäß aus zwei Teilen, nämlich aus einem Sandkern und einem damit verbundenen Stahlkern. Hierbei wird vorzugsweise lediglich der obere Teil des Gießkerns, also derjenige Bereich, der später einem Brennraum des Zylinders zugeordnet ist, aus Sand ausgebildet, wogegen ein unterer Bereich, also derjenige Bereich, der einer späteren Zylinderlauffläche zugeordnet ist, aus Stahl ausgebildet wird. Der Stahlkern nimmt dabei im Vergleich zum Sandkern deutlich mehr Wärme auf und führt diese vergleichsweise ab, wodurch es insbesondere im Bereich der Zylinderlauffläche zu einer deutlich erhöhten Temperaturdifferenz zwischen der Zylinderlauffläche (Oberfläche) und weiter innen kommt und dadurch Lunker vermieden bzw. zumindest reduziert werden können. Da derartige Lunker insbesondere im Bereich der späteren Zylinderlaufflächen äußerst kritisch sind, wird in besonders diesem Bereich der Stahlkern eingesetzt, um zusammen mit der außenliegenden und ebenfalls aus Metall ausgebildeten Kokille eine möglichst rasche/gleichmäßige Abkühlung des gegossenen Zylinders zu erreichen. Durch den aus Stahl ausgebildeten Kern erfolgt nun im Bereich der Zylinderlauffläche eine ebenso rasche Abkühlung nach innen wie nach außen zur Stahlkokille, wodurch die sich unter Umständen bildenden Lunker ins Innere der Zylinderwand gedrängt werden und zwar so tief, dass diese bei einer späteren Bearbeitung nicht mehr geöffnet werden. Im Bereich des späteren Brennraums hingegen ist der Gießkern weiterhin durch einen Sandkern gebildet, wodurch insbesondere schwierige Gießgeometrien, insbesondere auch Hinterschnitte, herstellbar sind. Der wesentliche Vorteil des erfindungsgemäßen Gießkerns liegt darin, dass die Lunkerbildung zumindest stark reduziert oder vorzugweise gänzlich vermieden wird und selbst beim Auftreten von Lunkern diese so tief in der Zylinderwand angeordnet sind, dass sie bei einem späteren Bearbeitungsschritt, bspw. bei einem Drehen oder Honen, nicht geöffnet werden und dadurch die Zylinderlaufeigenschaften nicht negativ beeinträchtigen. Erfindungsgemäß greift der Sandkern über einen Dorn in eine entsprechende Ausnehmung am Stahlkern ein. Der Sandkern ist dabei vorzugsweise formschlüssig mit dem Stahlkern verbunden, wodurch die Handhabbarkeit des aus dem Sandkern und dem Stahlkern gebildeten Gießkerns deutlich vereinfacht wird.
- Bei einer vorteilhaften Weiterbildung der erfindungsgemäßen Lösung sind/ist der Sandkern und/oder der Stahlkern jeweils massiv ausgebildet. Durch die massive Ausbildung des Sandkerns und/oder des Stahlkerns sind diese vergleichsweise robust und dadurch bestens geeignet für den Einsatz in modernen Gießereien. Zugleich ermöglicht eine massive Ausbildung, insbesondere des Stahlkerns, auch eine deutlich verbesserte Wärmeaufnahme und damit eine deutlich verbesserte Wärmeabfuhr, wodurch ein gleichmäßiges Erstarren bzw. Erkalten des Zylinders erreicht werden kann.
- Weitere wichtige Merkmale und Vorteile der Erfindung ergeben sich aus den Unteransprüchen, aus den Zeichnungen und aus der zugehörigen Figurenbeschreibung anhand der Zeichnungen.
- Es versteht sich, dass die vorstehend genannten und die nachstehend noch zu erläuternden Merkmale nicht nur in der jeweils angegebenen Kombination, sondern auch in anderen Kombinationen oder in Alleinstellung verwendbar sind, ohne den Rahmen der vorliegenden Erfindung zu verlassen.
- Bevorzugte Ausführungsbeispiele der Erfindung sind in den Zeichnungen dargestellt und werden in der nachfolgenden Beschreibung näher erläutert, wobei sich gleiche Bezugszeichen auf gleiche oder ähnliche oder funktional gleiche Bauteile beziehen.
- Dabei zeigen, jeweils schematisch,
- Fig. 1
- einen erfindungsgemäßen Gießkern in einer Ansicht,
- Fig. 2
- eine Schnittdarstellung durch den erfindungsgemäßen Gießkern entlang der Schnittebene A-A.
- Entsprechend den
Fig. 1 und 2 , weist ein erfindungsgemäßer Gießkern 1 einer im übrigen nicht dargestellten Gussform zur Herstellung eines ebenfalls nicht dargestellten Zylinders einer Brennkraftmaschine, insbesondere zur Herstellung eines Zylinders eines Zweitaktmotors, einen Sandkern 2 sowie einen damit verbundenen Stahlkern 3 auf. Demzufolge ist der Gießkern 1 zweiteilig ausgebildet, wobei der Sandkern 2 einen Bereich eines späteren Brennraums des Zylinders zumindest teilweise abdeckt, wogegen der Stahlkern 3 einen Bereich einer späteren Zylinderlauffläche zumindest teilweise abdeckt. Insbesondere im Bereich der späteren Zylinderlauffläche ist das Auftreten von Lunkern äußerst kritisch, da dadurch die Kolbenlaufeigenschaften negativ beeinträchtigt werden können. Es gilt demzufolge derartige Lunker unbedingt zu vermeiden. Solche Lunker entstehen insbesondere dadurch, dass der gegossene Zylinder ungleichmäßig und mit großen Temperaturdifferenzen erstarrt, was insbesondere bei der Verwendung von bisher üblichen und ganz aus Sand ausgebildeten Gießkernen an der Tagesordnung war. Hier kann der erfindungsgemäße Sandkern 1 Abhilfe schaffen, indem er im Bereich einer späteren Zylinderlauffläche aus dem Stahlkern 3 gebildet ist und dadurch eine vergleichsweise hohe Wärmeabfuhr ermöglicht. Die hohe Wärmeabfuhr insbesondere im Bereich der späteren Zylinderlauffläche bewirkt eine geringe Temperaturdifferenz des erkaltenden Zylinders zwischen dem innenliegenden Stahlkern 3 und der außenliegenden, nicht gezeigten Kokille. Die Kokille bildet dabei eine Außenform der Gussform, wogegen der Gießkern 1 die Innenform der Gussform darstellt. Gleichzeit drängt der Stahlkern 3 durch eine hohe Abkühlgeschwindigkeit die sich bildenden Lunker so tief ins Innere der Zylinderwand, dass sie auch bei einer späteren Bearbeitung nicht mehr geöffnet werden. - Durch die Ausbildung des Gießkerns 1 im Bereich des späteren Brennraums des Zylinders aus Sand bzw. aus dem erfindungsgemäßen Sandkern 2 ist es möglich, selbst komplizierte Geometrien in diesem Bereich, insbesondere auch Hinterschnitten, gießen zu können.
- Betrachtet man die
Fig. 2 , so kann man erkennen, dass der Sandkern 2 einen Dorn 4 aufweist, der in eine entsprechende Ausnehmung 5 am Stahlkern 3 eingreift. Selbstverständlich ist auch die Ausbildung eines derartigen Dorns 4 am Stahlkern 3 und die entsprechende Ausbildung der Ausnehmung 5 am Sandkern 2 denkbar. Über den Dorn 4 und die zugehörige Ausnehmung 5 kann eine formschlüssige Verbindung zwischen dem Sandkern 2 und dem Stahlkern 3 erreicht werden. - Wie der
Fig. 2 weiter zu entnehmen ist, sind/ist der Sandkern 2 und/oder der Stahlkern 3 massiv ausgebildet, wodurch insbesondere im Bereich des Stahlkerns 3 eine hohe und eine rasche Wärmeabfuhr erfolgen kann. Stahl besitzt dabei gegenüber Sand eine deutlich verbesserte Wärmeleitfähigkeit. Zusätzlich können im Stahlkern 3 Öffnungen 6 vorgesehen sein, über welche bspw. eine Entlüftung oder Kühlen erfolgen kann. - Der erfindungsgemäße Gießkern 1 wird zum Herstellen von gegossenen Zylindern benutzt und bei diesem Verfahren von einer nicht gezeigten Kokille umgeben. Zusammen mit der Kokille stellt der Gießkern die Gussform dar. Das zum Gießen des Zylinders verwendete Material kann bspw. Stahlguss aber auch Leichtmetall, wie bspw. Aluminium sein.
- Mit dem erfindungsgemäßen Gießkern 1 sind eine gleichmäßige Abkühlung des gegossenen Zylinders von innen und außen und damit verbunden eine deutlich reduzierte Lunkerbildung im Bereich der kritischen Bereiche zu erreichen, wodurch die Qualität der so hergestellten Zylinder deutlich gesteigert werden kann. Bilden sich wider Erwarten trotzdem Lunker bzw. Einschlüsse, so sind diese üblicherweise so tief im Zylinder angeordnet, dass sie bei einem späteren Bearbeitungsschritt, bspw. bei einem Schleifen, Drehen oder Honen, nicht offengelegt werden und dadurch unschädlich sind.
Claims (6)
- Gießkern (1) einer Gussform zur Herstellung eines Zylinders einer Brennkraftmaschine, insbesondere eines Zweitaktmotors,
wobei der Gießkern (1) zweiteilig ausgebildet ist, nämlich aus einem Sandkern (2) und einem damit verbundenen Stahlkern (3),
dadurch gekennzeichnet,
dass der Sandkern (3) über einen Dorn in eine entsprechende Ausnehmung (5) am Stahlkern (2) eingreift. - Gießkern nach Anspruch 1,
dadurch gekennzeichnet,
dass der Sandkern (2) einen Bereich des späteren Brennraums des Zylinders zumindest teilweise abdeckt, wogegen der Stahlkern (3) einen Bereich einer späteren Zylinderlauffläche zumindest teilweise abdeckt. - Gießkern nach Anspruch 1 oder 2,
dadurch gekennzeichnet,
dass der Sandkern (2) formschlüssig mit dem Stahlkern (3) verbunden ist. - Gießkern nach einem der Ansprüche 1 bis 3,
dadurch gekennzeichnet,
dass der Sandkern (2) und/oder der Stahlkern (3) massiv ausgebildet sind. - Verfahren zur Herstellung eines gegossenen Zylinders, bei dem eine Kokille als Außenform und ein Gießkern (1) nach einem der Ansprüche 1 bis 5 als Innenform eingesetzt werden.
- Verfahren nach Anspruch 5,
dadurch gekennzeichnet,
dass der zwischen der Außenform und der Innenform verbleibende Hohlraum mit Metall, insbesondere mit Aluminium ausgegossen wird.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102011079356A DE102011079356A1 (de) | 2011-07-18 | 2011-07-18 | Gießkern einer Gussform zur Herstellung eines Zylinders |
| PCT/EP2012/063048 WO2013010798A1 (de) | 2011-07-18 | 2012-07-04 | GIEßKERN EINER GUSSFORM ZUR HERSTELLUNG EINES ZYLINDERS |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2734322A1 EP2734322A1 (de) | 2014-05-28 |
| EP2734322B1 true EP2734322B1 (de) | 2017-09-06 |
Family
ID=46420236
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12731009.2A Not-in-force EP2734322B1 (de) | 2011-07-18 | 2012-07-04 | GIEßKERN EINER GUSSFORM ZUR HERSTELLUNG EINES ZYLINDERS |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP2734322B1 (de) |
| CN (1) | CN103648681B (de) |
| BR (1) | BR112014001061A2 (de) |
| DE (1) | DE102011079356A1 (de) |
| WO (1) | WO2013010798A1 (de) |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015225588A1 (de) | 2015-12-17 | 2017-06-22 | Volkswagen Aktiengesellschaft | Gießverfahren und Kühleinsatz zur Herstellung eines Gussteiles |
| US11654476B2 (en) | 2020-09-28 | 2023-05-23 | GM Global Technology Operations LLC | Hybrid core for manufacturing of castings |
| CN114406201B (zh) * | 2022-01-26 | 2023-11-14 | 阜新力达钢铁铸造有限公司 | 导轨无孔立柱的铸造方法及系统 |
Family Cites Families (25)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE719454C (de) * | 1940-06-30 | 1942-04-09 | Metallgussgesellschaft M B H | Verfahren und Vorrichtung zum Festhalten der Kuehleisen in Kern- oder Formkaesten |
| CH300083A (de) * | 1942-11-20 | 1954-07-15 | Daimler Benz Ag | Giessform mit Kernen zur Herstellung von Kurbelgehäusen von Brennkraftmaschinen. |
| GB1465486A (en) * | 1973-04-18 | 1977-02-23 | Aeroplane Motor Alu Cast | Method and apparatus for forming a curved passage in a casting and a casting so formed |
| US4003422A (en) * | 1975-04-21 | 1977-01-18 | Schramm Buford J | Process for making a composite cylinder head assembly |
| US4252175A (en) * | 1979-05-25 | 1981-02-24 | Outboard Marine Corporation | Cylinder block having a cast-in core unit and process for manufacturing same |
| CH640160A5 (de) * | 1979-07-05 | 1983-12-30 | Fischer Ag Georg | Kokille mit kernzug. |
| JPS6040663A (ja) * | 1983-08-11 | 1985-03-04 | Kawasaki Heavy Ind Ltd | シリンダブロツクの製造方法 |
| YU43348B (en) | 1984-03-13 | 1989-06-30 | Tam | Combined kernel for casting cylinders of grey cast iron for air cooled internal combustion motors |
| JPH03283Y2 (de) * | 1986-07-24 | 1991-01-08 | ||
| US4986942A (en) * | 1988-03-22 | 1991-01-22 | Outboard Marine Corporation | Method for forming ported cylinder sleeve liner foam pattern |
| JP2797187B2 (ja) * | 1988-06-06 | 1998-09-17 | 本田技研工業株式会社 | 2サイクルエンジン用シリンダブロックの鋳造方法 |
| DE59707494D1 (de) * | 1997-04-15 | 2002-07-18 | Waertsilae Schweiz Ag Winterth | Giessform und Verfahren zum Herstellen von metallischen Hohlgiesslingen sowie Hohlgiesslinge |
| JP2000126847A (ja) * | 1998-10-22 | 2000-05-09 | Daido Steel Co Ltd | 中空鋼塊の鋳造方法及びこの方法に使用する中子 |
| US6478073B1 (en) * | 2001-04-12 | 2002-11-12 | Brunswick Corporation | Composite core for casting metallic objects |
| US6527040B2 (en) * | 2001-06-11 | 2003-03-04 | General Motors Corporation | Casting of engine blocks |
| FR2841163B1 (fr) * | 2002-06-21 | 2005-01-28 | Montupet Sa | Procede de moulage de pieces de fonderie, notamment de blocs-moteurs, en alliage leger |
| JP3910955B2 (ja) * | 2003-12-22 | 2007-04-25 | 株式会社共立 | インサート中子及びそれを用いた内燃エンジン用シリンダの製造方法 |
| DE102005051561B3 (de) * | 2005-10-26 | 2007-01-11 | Honsel Gmbh & Co Kg | Verfahren und Anlage zum Gießen von Leichtmetall-Zylinderkurbelgehäusen in Sandformen |
| US7438117B2 (en) * | 2006-01-19 | 2008-10-21 | Gm Global Technology Operations, Inc. | Cylinder block casting bulkhead window formation |
| DE102006006132A1 (de) * | 2006-02-10 | 2007-08-16 | Hydro Aluminium Alucast Gmbh | Verfahren und Vorrichtung zum Montieren einer Gießform zum Gießen eines Gussteils aus einer Metallschmelze |
| DE102006053404A1 (de) * | 2006-11-10 | 2008-05-15 | Hydro Aluminium Alucast Gmbh | Gießform zum Gießen eines Gussteils und Verwendung einer solchen Gießform |
| DE102006058123A1 (de) * | 2006-12-09 | 2008-06-19 | Mahle International Gmbh | Formkörper zur Herstellung eines Hohlraumes |
| JP2008183581A (ja) * | 2007-01-29 | 2008-08-14 | Toyota Motor Corp | シリンダブロックの製造方法 |
| DE102010026597A1 (de) * | 2010-07-08 | 2012-01-12 | Mahle International Gmbh | Verfahren zur Herstellung eines Zylinders für einen Zweitaktmotor sowie Gusskern hierfür |
| CN102059321A (zh) * | 2010-12-10 | 2011-05-18 | 西安航空动力控制科技有限公司 | 一种型芯及其制备方法以及利用型芯制备铸件内腔的方法 |
-
2011
- 2011-07-18 DE DE102011079356A patent/DE102011079356A1/de not_active Withdrawn
-
2012
- 2012-07-04 WO PCT/EP2012/063048 patent/WO2013010798A1/de not_active Ceased
- 2012-07-04 BR BR112014001061A patent/BR112014001061A2/pt not_active Application Discontinuation
- 2012-07-04 EP EP12731009.2A patent/EP2734322B1/de not_active Not-in-force
- 2012-07-04 CN CN201280032924.9A patent/CN103648681B/zh not_active Expired - Fee Related
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2734322A1 (de) | 2014-05-28 |
| CN103648681B (zh) | 2016-07-13 |
| DE102011079356A1 (de) | 2013-01-24 |
| CN103648681A (zh) | 2014-03-19 |
| WO2013010798A1 (de) | 2013-01-24 |
| BR112014001061A2 (pt) | 2017-02-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2091678B1 (de) | Giessform zum giessen eines gussteils und verwendung einer solchen giessform | |
| DE102014101080B3 (de) | Vorrichtung zur Herstellung eines Zylinderkurbelgehäuses im Niederdruck- oder Schwerkraftgießverfahren | |
| WO2008138508A1 (de) | Verfahren zur herstellung eines zylinderkurbelgehäuses | |
| EP3347585B1 (de) | Kühlung eines kolbens mittels natriumgefüllter röhrchen | |
| DE102005047035B3 (de) | Verfahren zur Herstellung eines Kolbens für einen Verbrennungsmotor sowie danach hergestellter Kolben | |
| EP2129480B1 (de) | Anordnung und verfahren zum druckgiessen eines zylinderkurbelgehäuses | |
| EP0872295A1 (de) | Giessform und Verfahren zum Herstellen von metallischen Hohlgiesslingen sowie Hohlgiesslinge | |
| EP3310509B1 (de) | Hubkolben-verbrennungskraftmaschine und verfahren zum herstellen einer hubkolben-verbrennungskraftmaschine | |
| DE112005002155B4 (de) | Zylinderbohrungslaufbuchsen für gegossene Motorzylinderblöcke | |
| EP3377244B1 (de) | Gegossene zu- und ablauföffnungen bei stahlguss- und eisen-gusskolben | |
| DE102017204316A1 (de) | Verbrennungsmotor | |
| EP2738377B1 (de) | Verfahren zur Herstellung eines Zylinderkurbelgehäuses | |
| WO2013010798A1 (de) | GIEßKERN EINER GUSSFORM ZUR HERSTELLUNG EINES ZYLINDERS | |
| DE102013217251A1 (de) | Sandgiessen eines aluminiumdieselkolbens mit einer einspringenden brennraummulde im gusszustand für dieselmotoren für leichte oder mittlere beanspruchungen | |
| EP3097299A1 (de) | Verfahren zur herstellung eines kolbens für einen verbrennungsmotor | |
| DE102007060502B4 (de) | Verfahren zur Herstellung eines Zylinderkurbelgehäuses | |
| DE10003821C5 (de) | Kolben, insbesondere ein Leichtmetallkolben für eine Brennkraftmaschine | |
| EP3041623B1 (de) | Verfahren zum entformen eines aus leichtmetallschmelze gegossenen gussteils aus einer giessform | |
| DE10318778B4 (de) | Zylinderliner zum Eingießen in ein Zylindergehäuse | |
| WO2013139845A2 (de) | Verfahren zur herstellung eines gekühlten ringträgers | |
| DE102011100138A1 (de) | Zylindergehäuse | |
| EP1954424A1 (de) | Einteiliger stahlkolben als feinguss-variante mit kern für die feingusstechnische herstellung eines kühlkanales | |
| DE102008034462A1 (de) | Verfahren zum Gießen von Teilen | |
| DE102019106643A1 (de) | Wassermantelkern | |
| DE102009051269A1 (de) | Verfahren zur Herstellung von Zylinderkurbelgehäusen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20131219 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| 17Q | First examination report despatched |
Effective date: 20150424 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20170221 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: AT Ref legal event code: REF Ref document number: 925317 Country of ref document: AT Kind code of ref document: T Effective date: 20170915 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502012011200 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20170906 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171206 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171206 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180106 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502012011200 Country of ref document: DE |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| 26N | No opposition filed |
Effective date: 20180607 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20180725 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20180731 Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20180704 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180704 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20180731 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180704 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180704 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 925317 Country of ref document: AT Kind code of ref document: T Effective date: 20180704 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180704 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190705 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20120704 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170906 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170906 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190704 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20230719 Year of fee payment: 12 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502012011200 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250201 |