EP2595781B1 - Lamellenchleifscheibe und verfahren zur herstellung einer lamellenchleifscheibe mit einem tellerförmigen träger - Google Patents
Lamellenchleifscheibe und verfahren zur herstellung einer lamellenchleifscheibe mit einem tellerförmigen träger Download PDFInfo
- Publication number
- EP2595781B1 EP2595781B1 EP11734092.7A EP11734092A EP2595781B1 EP 2595781 B1 EP2595781 B1 EP 2595781B1 EP 11734092 A EP11734092 A EP 11734092A EP 2595781 B1 EP2595781 B1 EP 2595781B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- carrier
- support section
- adhesive
- grinding
- degrees
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Revoked
Links
- 238000004519 manufacturing process Methods 0.000 title claims description 14
- 238000000227 grinding Methods 0.000 claims description 44
- 241000446313 Lamella Species 0.000 claims description 16
- 230000004913 activation Effects 0.000 claims description 12
- 238000000034 method Methods 0.000 claims description 12
- 229920001169 thermoplastic Polymers 0.000 claims description 8
- 239000004416 thermosoftening plastic Substances 0.000 claims description 8
- 230000008569 process Effects 0.000 claims description 3
- 239000000126 substance Substances 0.000 claims description 3
- 238000005530 etching Methods 0.000 claims description 2
- 239000004838 Heat curing adhesive Substances 0.000 claims 4
- 239000000853 adhesive Substances 0.000 description 38
- 230000001070 adhesive effect Effects 0.000 description 38
- 229920001187 thermosetting polymer Polymers 0.000 description 15
- 230000008901 benefit Effects 0.000 description 5
- 229920002430 Fibre-reinforced plastic Polymers 0.000 description 2
- 239000000969 carrier Substances 0.000 description 2
- 230000008859 change Effects 0.000 description 2
- 239000011248 coating agent Substances 0.000 description 2
- 238000000576 coating method Methods 0.000 description 2
- 230000006378 damage Effects 0.000 description 2
- 230000001419 dependent effect Effects 0.000 description 2
- 239000002360 explosive Substances 0.000 description 2
- 239000011151 fibre-reinforced plastic Substances 0.000 description 2
- 239000003292 glue Substances 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 238000009966 trimming Methods 0.000 description 2
- 208000027418 Wounds and injury Diseases 0.000 description 1
- 238000004026 adhesive bonding Methods 0.000 description 1
- 238000000137 annealing Methods 0.000 description 1
- 230000000740 bleeding effect Effects 0.000 description 1
- 238000011109 contamination Methods 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 239000003822 epoxy resin Substances 0.000 description 1
- 239000000945 filler Substances 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 208000014674 injury Diseases 0.000 description 1
- 238000011068 loading method Methods 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
- 238000002156 mixing Methods 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 229920000647 polyepoxide Polymers 0.000 description 1
- 239000004848 polyfunctional curative Substances 0.000 description 1
- 238000005086 pumping Methods 0.000 description 1
- 230000035484 reaction time Effects 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000007788 roughening Methods 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 239000000758 substrate Substances 0.000 description 1
- 239000012815 thermoplastic material Substances 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D18/00—Manufacture of grinding tools or other grinding devices, e.g. wheels, not otherwise provided for
- B24D18/0072—Manufacture of grinding tools or other grinding devices, e.g. wheels, not otherwise provided for using adhesives for bonding abrasive particles or grinding elements to a support, e.g. by gluing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D13/00—Wheels having flexibly-acting working parts, e.g. buffing wheels; Mountings therefor
- B24D13/14—Wheels having flexibly-acting working parts, e.g. buffing wheels; Mountings therefor acting by the front face
- B24D13/16—Wheels having flexibly-acting working parts, e.g. buffing wheels; Mountings therefor acting by the front face comprising pleated flaps or strips
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D18/00—Manufacture of grinding tools or other grinding devices, e.g. wheels, not otherwise provided for
- B24D18/0045—Manufacture of grinding tools or other grinding devices, e.g. wheels, not otherwise provided for by stacking sheets of abrasive material
Definitions
- the invention relates to a method for producing a lamellar grinding wheel with a plate-shaped carrier, wherein a plurality of shingled overlapping grinding lamellae are adhesively bonded to an annular carrier section centered on the rotation axis of the lamellar grinding wheel, wherein the carrier section is made of an amorphous thermoplastic, in particular of ABS. Furthermore, the invention relates to a lamella grinding disc of the same type.
- Known lamella grinding wheels have a lamella carrier, which usually consists of woven or fiber-reinforced plastic or constructed of unreinforced thermoplastic material.
- the abrasive slats are glued from abrasive on a shingle overlapping.
- the support section carrying the slats is usually perpendicular to the axis of rotation.
- the support section is inclined in a special type of lamellar grinding wheel, so that the clamping screw stands out from the surface to be machined when the inclined grinding surface rests.
- the WO 2002/096603 A1 shows a lamellar grinding wheel with a carrier plate made of plastic.
- thermosetting epoxy resin-based system for bonding an amorphous thermoplastic support
- poor adhesion of the adhesive and thus of the fins to the support is shown. This leads to the release of the glue layer and the slats from the carrier, resulting in an increased risk of accidents.
- Thermosetting adhesives are thus far not suitable for the production of trimmable Lamelienschleifmissionn.
- the essential basic idea of the invention is to change the surface of the carrier section before gluing in such a way that a secure hold even of the thermosetting adhesive is ensured. This change is called activation and can be accomplished in various ways. After the activation according to the invention, the thermosetting adhesive is applied to the activated surface of the support section. On the provided with adhesive support section, the grinding blades are then placed and pressed.
- the main advantage is that the activation improves the adhesion of the thermosetting adhesive to the surface of the support.
- Activation in the sense of the application means a mechanical, physical and / or chemical treatment by which the surface is roughened or provided with a coating which improves the adhesion of the thermosetting adhesive.
- the roughening of the surface increases the available contact surface of the adhesive on the support section, the coating changes its properties.
- debris adhering to the surface is removed.
- Activation increases the adhesion of the adhesive to the surface.
- the surface of the carrier made of ABS is prepared by the activation according to the invention for the use of the thermosetting adhesive.
- the lamellar grinding wheel according to the invention has a significantly increased minimum explosive value.
- the required minimum explosive value of 140 m / s is clearly exceeded.
- the bonded abrasive slats are thus securely held on the activated support despite the use of a thermosetting adhesive.
- a flat detachment of the adhesive from the carrier is no longer observed.
- thermosetting adhesive also offers significant advantages in the production process of the lamella grinding wheels.
- a thermosetting adhesive cures significantly above room temperature, especially in a temperature range between 100 and 150 ° Celsius.
- the reaction of the adhesive and its reaction time are temperature dependent and thus can be controlled by temperature.
- thermosetting adhesive system in contrast to a cold-curing adhesive system, can already be introduced into the production process in ready-mixed form. A mixing chamber is no longer required.
- the adjustment of the viscosity by means of e.g. Fillers and / or the average molecular weight and the required homogeneity can already be set in the manufacture of the adhesive, ie before processing, at the supplier.
- thermosetting adhesive Due to the relatively high tolerance to heat, it is also possible to set the desired viscosity of the adhesive over the temperature.
- the thermosetting adhesive can be easily pumped and dosed in this way. Due to the rapid cooling on the plate carrier, the viscosity of the adhesive increases in a short time, so that the lamellae can be set handling-resistant and the glue does not run on the carrier.
- thermosetting systems can not cure in the production process during a longer standstill in the production process. A time-consuming and costly replacement of these components, such as the nozzle, after a stoppage of the production process is therefore not required.
- the activation of the surface of the support section is accomplished by abrading, chemical annealing or etching.
- abrading chemical annealing or etching.
- etching etching
- the activation of the surface according to the invention is preferably integrated directly in the production process.
- the activation of the surface can be automated, so that a reduction of the production output can be avoided despite the additional work to be performed.
- a very significant advantage of the invention lies in the fact that with the procedure according to the invention for the first time a trimmable, because on a thermoplastic plastic-building lamella grinding wheel can be produced with an inclined support portion.
- the support portion is inclined to the axis of rotation of the support at an angle between 50 and 85 degrees, in particular between 60 and 80 degrees.
- the thermosetting adhesive has a sufficiently high viscosity with sufficient adhesion at the stage of processing, so that the attached lamellae remain in their position and do not slip off the slope.
- Such lamella grinding wheels with an inclined support section have the great advantage that the possible contact surface and thus the largest material removal by the inclined against the rotation axis grinding surface is particularly large. Due to the oblique orientation and the possible higher contact surface results in a significant added value for the user of slats with oblique geometry.
- the individual sanding lamellae can be held in a manner resistant to handling during laying on the slope, and a bleeding of the adhesive before curing can be avoided.
- the cold-curing adhesive hitherto used for bonding substrates made of ABS is not suitable for bonding sanding disks to an obliquely oriented disk carrier.
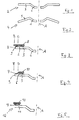
- FIG. 1 shows a schematic representation of a straight carrier 1 a lamellar grinding wheel 2.
- the carrier 1 is arranged symmetrically about an axis of rotation A and has a straight, that is perpendicular to the axis of rotation A directed carrier section 3.
- a support 4 is shown with the same axis of rotation A, the support portion 5 obliquely, in the illustrated case by approximately 70 degrees inclined to the rotation axis A, is aligned.
- FIG. 4 shows a schematic representation of a carrier 1 with a glued on the surface 6 of the support portion 5 with adhesive 7 individual grinding blade 8.
- the still unused grinding blade 8 is radially outward beyond the lateral surface 9 of the support portion 5 via. In the same way, it covers the adhesive 7 located between it and the support section 5.
- an area of the sanding lamella is available, which is outlined by the arrows B and C.
- the sanding lamella is worn beyond the above-mentioned range to the point marked with arrow D.
- the adhesive 7 and the carrier portion 3 project radially on the worn grinding blade 10.
- a part of the adhesive 7 has already been removed.
- the support portion 3 is dressed.
- the parts of the support section 3 and of the adhesive 7 projecting beyond the worn grinding lamella 10 are removed.
- the FIG. 5 shows such a trained support portion 11.
- the worn abrasive lamella 10 again protrudes on the support section.
- the thus-trained flap wheel 12 can be used further. The process can be repeated at will, so that the sanding disks can be used over their entire grinding surface.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Polishing Bodies And Polishing Tools (AREA)
- Making Paper Articles (AREA)
Description
- Die Erfindung betrifft ein Verfahren zur Herstellung einer Lamellenschleifscheibe mit einem tellerförmigen Träger, wobei eine Mehrzahl von sich schindelartig überlappenden Schleiflamellen auf einen ringförmigen auf die Rotationsachse der Lamellenschleifscheibe zentrierten Trägerabschnitt aufgeklebt werden, wobei der Trägerabschnitt aus einem amorphen Thermoplast, insbesondere aus ABS, gefertigt ist. Des Weiteren betrifft die Erfindung eine ebensolche Lamellenschleifscheibe.
- Bekannte Lamellenschleifscheiben weisen einen Lamellen-Träger auf, der üblicherweise aus gewebe- oder faserverstärkten Kunstoffen besteht oder aus unverstärktem thermoplastischen Material aufgebaut ist. Auf den Träger werden die Schleif-Lamellen aus Schleifmittel auf Unterlage schindelartig überlappend aufgeklebt. Bekanntermaßen ist der die Lamellen tragende Trägerabschnitt meist senkrecht zur Rotationsachse. Um besser flächig schleifen zu können, ist bei einer besonderen Art der Lamellenschleifscheibe der Trägerabschnitt schräg, so dass die Spannschraube bei Auflage der schrägen Schleiffläche sich quasi von der zu bearbeitenden Fläche abhebt. Die
WO 2002/096603 A1 zeigt eine Lamellenschleifscheibe mit einer Trägerplatte aus Kunststoff. - Beim Einsatz einer Lamellenschleifscheibe ist immer darauf zu achten, dass der Träger und/oder der unter den Schleif-Lamellen liegende Kleber nicht in Kontakt mit dem Werkstück kommt. Dies führt zu einer Verschmutzung oder Beschädigung des zu bearbeitenden Werkstückes. Solange die am Trägerabschnitt verklebten Schleif-Lamellen in radialer Richtung an der Mantelfläche des Trägers überstehen, schirmen sie das Werkzeug sicher vor einem Kontakt mit dem Träger ab. Allerdings lässt der Verschleiß der Schleif-Lamellen den Durchmesser der Lamellenschleifscheibe schrumpfen, so dass die Mantelfläche des Trägers unter den Schleif-Lamellen zum Vorschein kommt. In der Praxis kann somit meist nur ein Drittel des Lamellenbelages genutzt werden.
- Diesem Nachteil wird in der Praxis dadurch begegnet, dass das vom Träger überstehende Material abgetragen wird, indem dieser drehend an eine geeignete Kante gehalten wird. Diese Vorgehensweise ist als Abrichten oder Trimmen des Trägers bekannt. Durch das spanende Entfernen des überstehenden Teils ist ein Schleifen wieder möglich, ohne einen Kontakt des Trägers mit dem Werkstück befürchten zu müssen. Auf diese Weise kann ein wesentlich größerer Teil des Lamellenbelages genutzt werden. Um ein definiertes Trimmen mit Erhalt eines sauber abgedrehten Trägerrandes zu ermöglichen, werden statt der faserverstärkten Kunststoffe bekanntermaßen thermoplastische Kunststoffe, insbesondere amorphe Thermoplaste, wie ABS, für die Träger genutzt.
- Für das Bekleben solcher Träger aus amorphem Thermoplast werden bislang jedoch nur kalt aushärtende zwei Komponenten Klebstoffe verwendet, da diese Klebstoffe einen besonders guten Halt der Lamellen auf dem Träger gewährleisten. Diese Klebstoffe haben jedoch den Nachteil einer verhältnismäßig geringen Viskosität, die dazu beiträgt, dass die frisch aufgeklebten Schleiflamellen bei mechanischer Beaufschlagung oder bei unsachgemäßer Lagerung leicht verrutschen, solange der Kleber nicht durch ausgehärtet ist. Auf der anderen Seite ist die Einstellung einer ausreichend hohen Viskosität kaum möglich, da der Kleber gefördert und mit dem Härter vermischt werden muss. Auch kann die Viskosität zum Zwecke des besseren Pumpens und Dosierens nicht über einen Beheizung der Düse erniedrigt werden, da durch die Temperaturerhöhung eine Beschleunigung der Aushärtung stattfinden würde.
- Wird statt dessen zum Bekleben eines Trägers aus amorphen Thermoplast ein warmhärtendes System auf Epoxidharzbasis verwendet, zeigt sich eine schlechte Haftung des Klebers und damit der Lamellen auf dem Träger. Das führt zum Lösen der Leimschicht und der Lamellen vom Träger, woraus eine erhöhte Unfallgefahr resultiert. Warmhärtende Klebstoffe sind somit für die Herstellung von trimmbaren Lamelienschleifscheiben bislang nicht geeignet.
- Es stellt sich hieraus die Aufgabe, ein Verfahren zur Herstellung einer Lamellenschleifscheibe der eingangs genannten Art vorzuschlagen, bei dem die Lamellen auf dem Träger auf einfache und sichere Art und Weise befestigt werden können. Darüber hinaus ist es die Aufgabe der Erfindung, eine demgemäße Lamellenschleifscheibe vorzuschlagen,
- Diese Aufgaben werden gelöst von einem Verfahren mit den Merkmalen des Anspruchs 1 und von einer Vorrichtung mit den Merkmalen des Anspruchs 6. Weitere besonders bevorzugte Ausgestaltungen der Erfindung werden in den abhängigen Ansprüchen gebannt.
- Der wesentliche Grundgedanke der Erfindung liegt darin, die Oberfläche des Trägerabschnitts vor dem Bekleben so zu verändern, dass ein sicherer Halt auch des warmhärtender Klebstoffes gewährleistet ist. Diese Veränderung wird als Aktivierung bezeichnet und lässt sich auf verschiedene Weise bewerkstelligen. Nach der erfindungsgemäßen Aktivierung wird der warmhärtende Klebstoff auf die aktivierte Oberfläche des Trägerabschnittes aufgebracht. Auf den mit Kleber versehenen Trägerabschnitt werden dann die Schleiflamellen aufgesetzt und angedrückt.
- Der Hauptvorteil liegt darin, dass mit der Aktivierung die Haftung des warmhärtenden Klebstoffes auf der Oberfläche des Trägers verbessert wird. Unter einer Aktivierung im Sinne der Anmeldung ist eine mechanischen, physikalischen und/oder chemischen Behandlung zu verstehen, durch welche die Oberfläche aufgerauht oder mit einem die Haftung des warmhärtenden Klebstoffs verbesserten Beschichtung versehen wird. Das Aufrauen der Oberfläche erhöht die verfügbare Kontaktfläche des Klebstoffes auf dem Trägerabschnitt, das Beschichten verändert ihre Eigenschaften. Zusätzlich werden durch die Aktivierung an der Oberfläche anhaftende Fremdkörper entfernt. Durch die Aktivierung erhöht sich die Haftung des Klebstoffes auf der Oberfläche. Die Oberfläche des Trägers aus ABS wird durch die erfindungsgemäße Aktivierung auf den Einsatz des warmhärtenden Klebstoffes vorbereitet.
- In Folge weist die erfindungsgemäße Lamellenschleifscheibe einen deutlich erhöhten Mindestsprengwert auf. Beispielsweise wird bei einem Durchmesser der Lamellenschleifscheibe von 115 mm der geforderte Mindestsprengwert von 140 m/s deutlich überschritten. Die verklebten Schleif-Lamellen werden also trotz des Einsatzes eines warmhärtender Klebstoffs sicher auf dem aktivierten Träger gehalten. Außerdem ist ein flächiges Ablösen des Klebers vom Träger nicht mehr zu beobachten. Bei Überlastung lösen sich nur einzelne Schleif-Lamellen vom Trägerabschnitt, die nahezu kein Verletzungsrisiko darstellen.
- Die Verwendung des warmhärtenden Klebstoffes bietet darüber hinaus auch wesentliche Vorteile im Produktionsprozess der Lamellenschleifscheiben. Ein warmhärtender Klebstoff härtet deutlich oberhalb der Raumtemperatur aus, insbesondere in einem Temperaturbereich zwischen 100 und 150°Celsius. Die Reaktion der Klebstoffes und seine Reaktionszeit sind von der Temperatur abhängig und können folglich über die Temperatur gesteuert werden.
- Ein warmhärtendes Klebstoffsystem kann somit im Gegensatz zu einem kalthärtenden Klebstoffsystem bereits fertig gemischt in den Produktionsprozess eingegeben werden. Eine Mischkammer ist nicht mehr erfordenich. Die Einstellung der Viskosität mit Hilfe von z.B. Füllstoffen und/oder dem mittleren Molekulargewicht und die benötigte Homogenität können schon in der Herstellung des Klebers, also vor der Verarbeitung, beim Lieferanten eingestellt werden.
- Auf Grund der relativ hohen Toleranz gegen Wärme kann auch die Einstellung der gewünschten Viskosität des Klebstoffes über die Temperatur erfolgen. Der warmhärtende Klebstoff kann auf diese Weise problemlos gepumpt und dosiert werden. Durch die schnelle Abkühlung auf dem Lamellenträger erhöht sich die Viskosität des Klebstoffes in kurzer Zeit, so dass die Lamellen handlingsfest gesetzt werden können und der Leim auf dem Träger nicht verläuft.
- Ein weiterer Vorteil der warmhärtenden Systeme ist, dass diese bei einem längeren Stillstand im Produktionsprozess in den von ihnen durchlaufenen Komponenten nicht aushärten können. Ein zeit- und kostenintensiver Austausch dieser Komponenten, beispielsweise der Düse, nach einem Stillstand des Produktionsprozesses ist somit nicht erforderlich.
- In einer bevorzugten Ausführungsform erfolgt die Aktivierung der Oberfläche des Trägerabschnitts durch ein Anschleifen, ein chemisches Anlösen oder Anätzen. Jede dieser Aktivierungsmethoden lässt sich leicht automatisieren und ist damit für eine Massenproduktion von Lamellenschleischeiben geeignet.
- Die erfindungsgemäße Aktivierung der Oberfläche wird vorzugsweise direkt im Produktionsprozess integriert. Das Aktivieren der Oberfläche ist automatisierbar, so dass trotz des zusätzlich auszuführenden Arbeitsschritts eine Verminderung des Produktionssausstoßes vermieden werden kann.
- Ein ganz wesentlicher Vorteil der Erfindung liegt nun darin, dass mit der erfindungsgemäßen Vorgehensweise zum ersten mal eine trimmbare, weil auf einem thermoplastischen Kunststoff aufbauende Lamellenschleifscheibe mit schrägem Trägerabschnitt hergestellt werden kann. Bei dieser ist der Trägerabschnitt zur Rotationsachse des Trägers hin in einem Winkel zwischen 50 und 85 Grad, insbesondere zwischen 60 und 80 Grad, geneigt. Dies ist nun möglich, weil der warm härtende Klebstoff eine ausreichend hohe Viskosität bei ausreichender Klebkraft im Stadium der Verarbeitung hat, so dass die aufgesetzten Lamellen in ihrer Position verbleiben und nicht von der Schräge abrutschen. Solche Lamellenschleifscheiben mit schrägem Trägerabschnitt haben den großen Vorteil, dass die mögliche Auflagefläche und damit der größte Materialabtrag durch den gegen die Rotationsachse geneigte Schleiffläche besonders groß ist. Durch die schräge Ausrichtung und die mögliche höhere Auflagefläche ergibt sich ein deutlicher Mehrwert für den Benutzer von Lamellenscheiben mit schräger Geometrie.
- Mit dem erfindungsgemäß genutzten Klebstoff hoher Viskosität können die einzelnem Schleif-Lamellen beim Legen auf der Schräge handlingsfest gehalten und ein Verlaufen des Klebstoffes vor dem Aushärten vermieden werden. Im Gegensatz zu dem erfindungsgemäßen Einsatz eines warmhärtenden Klebstoffs ist der bisher zum Bekleben von Trägern aus ABS verwendete, kalt aushärtende Klebstoff nicht geeignet, Schleif-Lamellen auf einen schräg ausgerichteten Lamellenträger zu kleben.
- Im Folgenden werden anhand der
Figuren 1 bis 5 verschiedene Verschleißzustände einer Lamellenschleifscheibe beschrieben. Dabei zeigt. - Figur 1:
- eine schematische Darstellung eines Trägers einer Lamellenschleifscheibe mit einem gerade ausgerichteten Trägerabschnitt;
- Figur 2:
- eine schematische Darstellung eines Trägers einer Lamellenschleifscheibe mit einem schräg ausgerichteten Trägerabschnitt;
- Figur 3:
- eine schematische Darstellung eines gerade ausgerichteten Trägers mit einer aufgeklebten Schleif-Lamelle im Neuzustand;
- Figur 4:
- eine schematische Darstellung eines gerade ausgerichteten Trägers mit einer verbrauchten Schleif-Lamelle;
- Figur 5:
- eine schematische Darstellung eines gerade ausgerichteten Trägers mit einem getrimmten Trägerabschnitt.
- Die
Figur 1 zeigt eine schematische Darstellung eines geraden Trägers 1 einer Lamellenschleifscheibe 2. Der Träger 1 ist symmetrisch um eine Rotationsachse A angeordnet und weist einen gerade, d.h. senkrecht zur Rotationsachse A hin ausgerichteten Trägerabschnitt 3 auf. In derFigur 2 wird ein Träger 4 mit gleicher Rotationsachse A gezeigt, dessen Trägerabschnitt 5 schräg, im dargestellten Fall um ca. 70 Grad gegen die Rotationsachse A geneigt, ausgerichtet ist. - Die verschiedenen Gebrauchsstadien einer Lamellenschleifscheibe mit einem trimmbaren Träger werden in den weiteren Figuren exemplarisch an einem gerade ausgerichteten Träger dargestellt, sind aber auf eine Lammellenschleifscheibe mit schräg ausgerichtetem Trägerabschnitt übertragbar.
-
Figur 4 zeigt eine schematische Darstellung eines Trägers 1 mit einer auf der Oberfläche 6 des Trägerabschnitts 5 mit Klebstoff 7 aufgeklebten einzelnen Schleif-Lamelle 8. Die noch unbenutzte Schleif-Lamelle 8 steht radial nach außen über die Mantelfläche 9 des Trägerabschnitts 5 über. Auf gleiche Weise überdeckt sie den sich zwischen ihr und dem Trägerabschnitt 5 sich befindenden Klebstoff 7. Für die Bearbeitung eines Werkstücks steht ein Bereich der Schleif-Lamelle zur Verfügung, der von den Pfeilen B und C umrissen wird. - In der
Figur 5 ist die Schleif-Lamelle nach Gebrauch über den oben genannten Bereich hinaus bis zum dem mit Pfeil D markierten Punkt abgetragen. Der Klebstoff 7 und der Trägerabschnitt 3 stehen radial an der abgenutzten Schleif-Lamelle 10 vor. Ein Teil des Klebstoffs 7 ist bereits abgetragen. Die Gefahr besteht, dass bei einem weiteren Gebrauch der Lamellenschleifscheibe auch zu einem Kontakt des Werkstückes mit der Mantelfläche 9 des überstehenden Trägerabschnitts 3 kommt. Um dies zu verhindern, wird der Trägerabschnitt 3 abgerichtet. Dabei werden die an der abgenutzten Schleif-Lamelle 10 überstehenden Teile des Trägerabschnitts 3 und des Klebstoffes 7 entfernt. DieFigur 5 zeigt einen derart abgerichteten Trägerabschnitt 11. Nach dem Abtrag der radial nach außen über die abgenutzte Schleif-Lamelle 10 hinaus stehenden Teile des Trägerabschnitts 3 und des Klebstoffs 7 steht die abgenutzte Schleif-Lamelle 10 wieder am Trägerabschnitt vor. Die derart abgerichtete Lamellenschleifscheibe 12 kann weiter genutzt werden. Der Vorgang ist beliebig wiederholbar, so dass die Schleif-Lamellen über ihre gesamte Schleiffläche genutzt werden können.
Claims (6)
- Verfahren zur Herstellung einer Lamellenschleifscheibe (4) mit einem tellerförmigen Träger, wobei eine Mehrzahl von sich schindelartig überlappenden Schleiflamellen (7) auf einen ringförmigen auf eine Rotationsachse (A) der Lamellenschleifscheibe (4) zentrierten Trägerabschnitt (3, 5) aufgeklebt werden, wobei der Trägerabschnitt (3, 5) aus einem amorphen Thermoplast, insbesondere aus ABS, gefertigt ist,
dadurch gekennzeichnet,
dass die Oberfläche (6) des Trägerabschnitts (3, 5) vor dem Bekleben aktiviert wird, dass ein warmhärtender Klebstoff (7) auf die aktivierte Oberfläche (6) des Trägerabschnittes aufgebracht wird und dass die Schleiflamellen (8) auf den mit warmhärtenden Klebstoff (7) versehenen Trägerabschnitt (5) aufgesetzt und angedrückt werden. - Verfahren nach Anspruch 1,
dadurch gekennzeichnet,
dass die Aktivierung der Oberfläche (6) durch ein Anschleifen, ein chemisches Anlösen oder ein Anätzen erfolgt. - Verfahren nach einem der Ansprüche 1 oder 2,
dadurch gekennzeichnet,
dass die Aktivierung der Oberfläche (6) der Belegung mit Schleiftamellen (7) unmittelbar vorausgeht und somit in den Prozess integriert ist. - Verfahren nach einem der vorherigen Ansprüche,
dadurch gekenntzeichnet,
dass der warmhärtende Klebstoff (7) auf die Oberfläche (6) eines Trägerabschnitt (5) aufgetragen wird, der zur Rotationsachse (A) des Trägers (1) hin zwischen 50 und 85 Grad, insbesondere zwischen 60 und 80 Grad, geneigt ist. - Lamellenschleifscheibe (4), insbesondere hergestellt mit einem Verfahren der Ansprüche 1 bis 5, aufweisend einen tellerförmigen Träger (1) der eine Vielzahl von sich schindelartig überlappenden Schleiflamellen (8) trägt, wobei die Schleiflamellen (8) auf einem Trägerabschnitt (3, 5) aufgeklebt sind, und wobei der Trägerabschnitt (3, 5) aus einem amorphen Thermoplast, insbesondere aus ABS, gefertigt ist,
dadurch gekennzeichnet,
dass die Schleiflamellen (8) mit einem warmhärtenden Klebstoff (7) auf dem Trägerabschnitt (3, 5) aufgeklebt sind. - Lamellenschleifscheibe (4) nach Anspruch 6,
dadurch gekennzeichnet,
dass der Trägerabschnitt (5) zur Rotationsachse (A) des Trägers (1) hin zwischen 50 und 85 Grad, insbesondere zwischen 60 und 80 Grad, geneigt ist.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102010031900 | 2010-07-21 | ||
| DE102011107675A DE102011107675A1 (de) | 2010-07-21 | 2011-07-13 | Verfahren zur Herstellung einer Lamellenschleifscheibe mit einem tellerförmigen Träger |
| PCT/EP2011/062377 WO2012010605A1 (de) | 2010-07-21 | 2011-07-19 | Lamellenschleifscheibe und verfahren zur herstellung einer lamellenschleifscheibe mit einem tellerförmigen träger |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2595781A1 EP2595781A1 (de) | 2013-05-29 |
| EP2595781B1 true EP2595781B1 (de) | 2014-08-27 |
Family
ID=44532793
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP11734092.7A Revoked EP2595781B1 (de) | 2010-07-21 | 2011-07-19 | Lamellenchleifscheibe und verfahren zur herstellung einer lamellenchleifscheibe mit einem tellerförmigen träger |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US20130115864A1 (de) |
| EP (1) | EP2595781B1 (de) |
| CN (1) | CN102971112A (de) |
| BR (1) | BR112013001228A2 (de) |
| DE (1) | DE102011107675A1 (de) |
| MX (1) | MX2012014804A (de) |
| WO (1) | WO2012010605A1 (de) |
Family Cites Families (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5233719A (en) * | 1988-04-27 | 1993-08-10 | Minnesota Mining And Manufacturing Co. | Apparatus and brush segment arrangement for finishing wheel brushes |
| JP2682844B2 (ja) * | 1988-06-20 | 1997-11-26 | 裕一 市口 | 研磨具の製造方法及びその装置 |
| DE3839238A1 (de) * | 1988-11-21 | 1990-05-23 | Leurop Leutheusser Kg | Faecherschleifscheibe |
| CN1035366C (zh) * | 1991-08-17 | 1997-07-09 | 格尔德艾森布拉特有限公司 | 端面为扇形叠片状的研磨工具 |
| DE9216621U1 (de) * | 1992-12-05 | 1993-01-28 | Lukas-Erzett Vereinigte Schleif- und Fräswerkzeugfabriken GmbH & Co KG, 5250 Engelskirchen | Schleifwerkzeug |
| DE69502187T2 (de) * | 1994-03-03 | 1998-10-15 | Minnesota Mining & Mfg | Verfahren zum Verbessern der Glätte einer Oberfläche |
| US5996167A (en) * | 1995-11-16 | 1999-12-07 | 3M Innovative Properties Company | Surface treating articles and method of making same |
| US5722881A (en) * | 1996-08-30 | 1998-03-03 | Merit Abrasive Products, Inc. | Flap wheel |
| GB2349109B (en) * | 1999-04-23 | 2002-09-04 | Elliott Ind Ltd | Improvements in or relating to abrasive flap discs |
| US6592442B2 (en) * | 2001-01-02 | 2003-07-15 | Jason Incorporated | Flap wheel |
| US6863596B2 (en) * | 2001-05-25 | 2005-03-08 | 3M Innovative Properties Company | Abrasive article |
| DK176743B1 (da) * | 2003-04-25 | 2009-06-02 | Flex Trim As | Slibeskive med sandpapiremner |
| DE202004004027U1 (de) * | 2004-03-12 | 2005-07-28 | RHODIUS Oualitätsschleifmittel GmbH & Co KG | Fächerschleifscheibe |
| US7207876B2 (en) * | 2004-06-17 | 2007-04-24 | Jason Incorporated | Flap wheel and method |
| DE102006024015A1 (de) * | 2006-05-23 | 2007-11-29 | August Rüggeberg Gmbh & Co. Kg | Fächer-Schleifscheibe |
| DE102006043989A1 (de) * | 2006-09-19 | 2008-03-27 | Gerd Eisenblätter Gmbh | Lamellenschleifscheibe |
| DE202009003323U1 (de) * | 2008-09-23 | 2010-03-25 | Mb Maschinenbau Gmbh | Schleifband für Schleifmaschinen |
-
2011
- 2011-07-13 DE DE102011107675A patent/DE102011107675A1/de not_active Withdrawn
- 2011-07-19 EP EP11734092.7A patent/EP2595781B1/de not_active Revoked
- 2011-07-19 WO PCT/EP2011/062377 patent/WO2012010605A1/de not_active Ceased
- 2011-07-19 US US13/811,302 patent/US20130115864A1/en not_active Abandoned
- 2011-07-19 BR BR112013001228A patent/BR112013001228A2/pt not_active IP Right Cessation
- 2011-07-19 MX MX2012014804A patent/MX2012014804A/es not_active Application Discontinuation
- 2011-07-19 CN CN2011800333042A patent/CN102971112A/zh active Pending
Also Published As
| Publication number | Publication date |
|---|---|
| CN102971112A (zh) | 2013-03-13 |
| WO2012010605A1 (de) | 2012-01-26 |
| BR112013001228A2 (pt) | 2016-06-07 |
| MX2012014804A (es) | 2013-04-29 |
| EP2595781A1 (de) | 2013-05-29 |
| DE102011107675A1 (de) | 2012-01-26 |
| US20130115864A1 (en) | 2013-05-09 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE60223139T2 (de) | Schleifscheibe und verbindungselement | |
| DE102009008881B4 (de) | Drehschleifstein und Verfahren zu seiner Herstellung | |
| DE19959347A1 (de) | Klebefolie zur Geräusch- und Stossabsorption, dieselbe verwendendes Sägeblatt sowie Herstellungsverfahren hierfür | |
| CH359376A (de) | Schleifvorrichtung, Verwendung der Schleifvorrichtung und Verfahren zu ihrer Herstellung | |
| EP0158200A2 (de) | Profilschleifscheibe | |
| WO2015067377A1 (de) | Vulkanfiber-schleifwerkzeug | |
| DE2740891C3 (de) | Umfangsschleifscheibe | |
| EP3651936B1 (de) | Fächerschleifscheibe für einen winkelschleifer | |
| EP2595781A1 (de) | Lamellenschleifscheibe und verfahren zur herstellung einer lamellenschleifscheibe mit einem tellerförmigen träger | |
| EP0348846A2 (de) | Ausgewuchtetes Lüfterrad sowie Verfahren und Vorrichtung zur Herbeiführung des Unwuchtausgleiches | |
| DE102009025116A1 (de) | Schleif-und/oder Polierwerkzeug und Herstellverfahren | |
| EP3191257B1 (de) | Werkzeug zur oberflächenfeinbearbeitung | |
| DE202007007839U1 (de) | Lamellenschleifscheibe | |
| EP1951476A1 (de) | Trennscheibe | |
| DE102011008044B4 (de) | Schleifscheibe | |
| DE19511004C1 (de) | Werkzeug mit einem Schleif- oder Polierbelag | |
| EP0799111B1 (de) | Recyclefähige schleifkörperzonen | |
| EP1138440A2 (de) | Schleifwerkzeug und Verfahren zu seiner Herstellung | |
| EP0657251B1 (de) | Trenn-Schleifscheibe für stationäre Schleifmaschinen und deren Verwendung | |
| EP3075808A1 (de) | Kunststoffkleber- oder kunststoffbauteilherstellungsverfahren sowie herstellungsanordnung | |
| DE102008027141A1 (de) | Schleifscheibe | |
| EP3906833B1 (de) | Reinigungsscheibe sowie verfahren zu deren herstellung | |
| AT202481B (de) | Schleifscheibe und Verfahren zu ihrer Herstellung | |
| DE3790060C2 (de) | ||
| DE102008029619B4 (de) | Trennschleifscheibe zur Erzeugung eines breiten Schnittes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20121126 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20140422 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 684269 Country of ref document: AT Kind code of ref document: T Effective date: 20140915 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502011004208 Country of ref document: DE Effective date: 20141009 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20140827 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141127 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141128 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141127 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141229 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141227 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R026 Ref document number: 502011004208 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| 26 | Opposition filed |
Opponent name: JOBRA METALL GMBH Effective date: 20150522 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20150722 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| RDAF | Communication despatched that patent is revoked |
Free format text: ORIGINAL CODE: EPIDOSNREV1 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R064 Ref document number: 502011004208 Country of ref document: DE Ref country code: DE Ref legal event code: R103 Ref document number: 502011004208 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20150719 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150719 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150731 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150731 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150719 |
|
| RDAG | Patent revoked |
Free format text: ORIGINAL CODE: 0009271 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20160331 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT REVOKED |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150731 |
|
| 27W | Patent revoked |
Effective date: 20160129 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MA03 Ref document number: 684269 Country of ref document: AT Kind code of ref document: T Effective date: 20160129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20110719 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140827 |