EP1524925B1 - Semelle - Google Patents
Semelle Download PDFInfo
- Publication number
- EP1524925B1 EP1524925B1 EP03766298A EP03766298A EP1524925B1 EP 1524925 B1 EP1524925 B1 EP 1524925B1 EP 03766298 A EP03766298 A EP 03766298A EP 03766298 A EP03766298 A EP 03766298A EP 1524925 B1 EP1524925 B1 EP 1524925B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- insole
- insole according
- layer
- fleece
- wad
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images


Classifications
-
- A—HUMAN NECESSITIES
- A43—FOOTWEAR
- A43B—CHARACTERISTIC FEATURES OF FOOTWEAR; PARTS OF FOOTWEAR
- A43B17/00—Insoles for insertion, e.g. footbeds or inlays, for attachment to the shoe after the upper has been joined
- A43B17/003—Insoles for insertion, e.g. footbeds or inlays, for attachment to the shoe after the upper has been joined characterised by the material
-
- A—HUMAN NECESSITIES
- A43—FOOTWEAR
- A43B—CHARACTERISTIC FEATURES OF FOOTWEAR; PARTS OF FOOTWEAR
- A43B17/00—Insoles for insertion, e.g. footbeds or inlays, for attachment to the shoe after the upper has been joined
- A43B17/10—Insoles for insertion, e.g. footbeds or inlays, for attachment to the shoe after the upper has been joined specially adapted for sweaty feet; waterproof
- A43B17/102—Moisture absorbing socks; Moisture dissipating socks
- A43B17/105—Disposable
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/24—Structurally defined web or sheet [e.g., overall dimension, etc.]
- Y10T428/24479—Structurally defined web or sheet [e.g., overall dimension, etc.] including variation in thickness
Definitions
- the invention relates to an insole for shoes as a disposable product, with a thickness of at most 3 mm, with a liquid-absorbent fiber fleece layer with or based on cellulosic fiber material.
- a sol sole is for example off DE 3215526 A known.
- EP 0 033 448 A1 is an insole made of an absorbent paper material with bactericidal and / or fungicidal and / or odor-controlling active ingredients known.
- EP 0 216 727 A2 discloses and teaches an insole of at least four plies, namely a non-slip bottom foam pad, a nonwoven intermediate layer thereon, an absorbent layer of multi-ply batting material and a cover layer, again of nonwoven fabric.
- the present invention has for its object to propose an insole that is technically simple and economical to produce and which is characterized by good performance characteristics.
- An insole according to the invention advantageously has a thickness of 1 to 3 mm, in particular of 1.1 to 1.4 mm, wherein the thickness is determined under a test pressure of 20 g / cm 2 .
- the specimens are previously stored for 24 hours at 105 ° C in a drying oven and then allowed to cool in a desiccator. Then they are weighed and then under the said test pressure of 20 g / cm 2 of their Thickness measured.
- embossing calendering the cotton fleece layer Kalander josughalzen be used with the embossment pattern forming elevations make up their share 8 to 20%, in particular 10 to 16% of the roll surface or the surface of the insole.
- the engraving depth and thus the height of the elevations is at least 0.5 mm.
- Smallest dimensions of the elevations or of the embossing structures formed thereby from 0.3 to 0.6 mm have proven to be advantageous and preferred. It may also be punctiform structures or elongate webs in the calender roll, which then form elongated highly compressed embossed areas of a longitudinal extension of a few millimeters, in particular 2 to 6 mm in length.
- the maximum tensile force in an insole according to the invention in the longitudinal direction in the dry state is advantageously 35 to 100 N / 25 mm, in particular 50 to 80 N / 25 mm and in the transverse direction 40 to 100 N / 25 mm, in particular 55 to 80 N / 25 mm.
- This maximum tensile force can be determined using a standardized tensile testing machine according to DIN 51221. Samples with a clamping width of 25 mm and a clamping length of 30 mm are taken from the stamped calendered cotton fleece layer to be tested.
- the clamped in clamping receptacles of the standardized tensile tester samples are then moved at a test speed of 100 mm / min in the plane of their extension and thereby the tensile force acting in this direction is measured.
- the maximum tensile force is meant the maximum force at which the cotton pad tears. If previously higher force peaks are measured in the course of stretching, these represent the maximum tensile force in the sense of this test.
- the insole according to the invention has a maximum tensile force in the wet state, which is 20 to 80 N / 25 mm, in particular 35 to 70 N / 25 mm in the longitudinal direction and 30 to 80, in particular 40 to 55 N / 25 mm in the transverse direction.
- a maximum tensile force in the wet state which is 20 to 80 N / 25 mm, in particular 35 to 70 N / 25 mm in the longitudinal direction and 30 to 80, in particular 40 to 55 N / 25 mm in the transverse direction.
- the sample thus obtained is placed in a wire basket and loaded with a flat steel plate (100 ⁇ 100 ⁇ 2 mm).
- the wire basket is immersed in the demineralized water together with the sample and the plate.
- the sample remains therein under the load of the plate for 30 sec.
- the plate is then lifted and the sample remains in the liquid for another 30 seconds without this load.
- the wire basket is then removed from the liquid along with the sample, and the liquid is allowed to drip over a corner for 120 seconds.
- the sample is then weighed again (M2).
- the water absorption capacity is then according to the DIN standard 53923 calculated according to (M2 - M1) / M1 x 100 in percent.
- the two auxiliary sheets are clamped in the tensile testing machine and then moved apart at a speed of 100 mm / min.
- the maximum tensile force is determined. Again, the maximum tensile force is understood as the maximum force at which the cohesion of the cotton pad is destroyed. If previously higher force peaks are measured in the course of stretching, these represent the maximum tensile force in the sense of this test.
- a section of the above-mentioned double-sided adhesive tape is adhesively bonded at the top and bottom of the cotton fleece layer of the insole according to the invention or another sole to be tested. It is expediently first of a laminate Cotton fleece layer or insole and tape formed and then punched out of this laminate round cotton wool pads with double-sided adhesive tape. The composite thus obtained is arranged (after removal of the outer cover layers of the adhesive tape) between the two auxiliary sheets and positioned centrically. Then the auxiliary sheets are weighted with 30 kg for 2 minutes, so that the composite of insole and double-sided adhesive tape and auxiliary sheets is intimately connected.
- This composite is then clamped in the tensile testing machine according to DIN 51221, and at the mentioned speed of 100 mm / min, the clamps are pulled apart, thereby determining the tensile force. From at least five individual measurements, the mean value is formed and given in N.
- the adhesive strength of the double-sided adhesive tape is specified or standardized according to the abovementioned stripping method of the German Pharmacopoeia 1996.
- the force required to peel tapes (e.g., patches) from a flat surface at an angle of 180 ° at a constant speed is measured.
- a tensile testing machine according to DIN 51221 class 1 is used for this purpose.
- strips of 400 mm length and given width of the roll of 12.5 or 25 mm are cut and applied to the cleaned metal plates so as to avoid trapped air.
- a "tape applicator” the tape strip is rolled under a pressure of 20 N / cm sample width (the back cover paper of the adhesive tape has not yet been removed). After 10 minutes waiting time then the measurement takes place.
- the upper free end of the sample strip is knocked back and withdrawn about 25 mm from the top of the steel plate.
- This end of the steel plate is clamped in the upper clamp of the tensile testing machine and the struck end of the sample strip is clamped in the lower clamp of the tensile tester.
- the take-off angle is therefore 180 °, whereby care must be taken that the sample backs are parallel to each other, but not rub against each other.
- the tensile testing machine is set to a take-off speed of 300 +/- 30 mm / min.
- the result shall be expressed as the mean of at least five tests in N / 25 mm rounded to one decimal place.
- the evaluation can also be done with a suitable PC program respectively.
- the above description of the adhesive strength serves to provide standardized reproducible conditions for the adhesive tape to be used in the above-described inner strength test.
- the insole according to the invention also proves advantageous in an abrasion test using a Crockmeter (a rubbing device) as described in DIN EN ISO 105-1212.
- a Crockmeter a rubbing device
- a nonwoven layer is rubbed with a defined standard test fabric.
- the resulting damage to the sample surfaces is assessed visually.
- three sections of 14 ⁇ 5 cm are taken from the fleece to be tested, with the longer side running in the machine direction.
- the journal of the mentioned grater is covered with the friction cloth.
- a test fabric, namely fine rib from the company Schiesser No. 4467 was used.
- the sample is fixed by means of retaining clips on said grater.
- the pin Over a distance of 10 cm, the pin is then moved back and forth until the first lint forms. After a total of 10 scrub cycles, the first visual assessment of the sample surface is made, after 30 cycles the second evaluation follows.
- the load of the pin is 400 g / cm 2 .
- the friction fabric When tested in the wet state, the friction fabric is adjusted to 100% moisture absorption, whereby the moistening in accordance with DIN EN ISO 105-x12.
- FIG. 1 shows in perspective view an embodiment of an insole 2 according to the invention.
- the insole 2 is formed from a single cotton fleece layer 4 of 50 wt .-% cotton fibers and 50 wt .-% polyethylene / polypropylene bicomponent fibers (PE / PP).
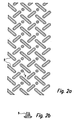
- the batt layer 4 is solidified by being emboss-calendered, that is, passed between a heated calender roll having projecting embossing protrusions and a counter pressure roll. In this way, the surface structure apparent from the figure was formed with punctiform and ridge-shaped embossed structures 6 in the illustrated case.
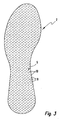
- FIG. 3 shows in plan view a FIG. 2 similar surface structure also obtained by embossing calendering in a like in FIG. 1 2.
- the elevations on the calender roll formed highly compressed embossed regions 9, in addition to regions 10 which are less densified.
- the proportion of high-density regions 9, in the total area, in this case amounts to 10 to 11%.
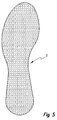
- FIGS. 4 and 5 show further embossed structures, which have proven to be advantageous in the production of an insole according to the invention.
- the pressing surface portion is at FIG. 4 about 12.5% and at FIG. 5 about 13.3%.
- the basis weight of the cotton fleece layer is 200-500 g / m 2 .
- the densification of the cotton batt layer by embossing calendering is such that a density of the entire batt fabric layer between 0.1 to 0.5 g / cm 3 , preferably between 0.2 and 0.3 g / cm 3 results, the specimens in sections of 100 x 100 mm initially stored for 24 hours at 105 ° C in a drying oven and then allowed to cool in a desiccator. They were then weighed to the nearest 0.1 g. Then, in a thickness gauge under a test pressure of 20 g / cm 2, the thickness of the specimens was measured to the nearest 0.1 mm, and then the density was calculated therefrom.
- the complex solution may contain a fungicidal active ingredient, e.g. Undecylenamide (DEA) can be added.
- a fungicidal active ingredient e.g. Undecylenamide (DEA) can be added.
- DEA Undecylenamide
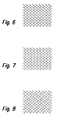
- FIGS. 6, 7 and 8 show different surface structures in the insole according to the invention, wherein it is at FIG. 6 around a surface texture like in FIG. 3 shown acts.
- the surface structure after FIGS. 7 and 8 differ slightly from this.
- the arrangement and dimensioning of the highly compressed embossed regions 9 and of the less densely compressed regions 10 can also be seen in an enlarged detail.
- the only cotton fleece layer 4 has been embossing calendered under an embossing pressure of 400 N / mm. Based on a weight per unit area of 303 g / m 2, this results in a nonwoven thickness in the embossed calendered state of the insole of 1.28 mm. A maximum dry tensile strength of 54.6 N / 25 mm in the longitudinal direction and 68.9 N / 25 mm in the transverse direction was determined. The water holding capacity was 1.7 g of liquid per g of cotton fleece layer.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Wood Science & Technology (AREA)
- Footwear And Its Accessory, Manufacturing Method And Apparatuses (AREA)
- Shaping Of Tube Ends By Bending Or Straightening (AREA)
- Nonwoven Fabrics (AREA)
- Saccharide Compounds (AREA)
- Transition And Organic Metals Composition Catalysts For Addition Polymerization (AREA)
- External Artificial Organs (AREA)
- Laminated Bodies (AREA)
Claims (13)
- Semelle orthopédique (2) pour chaussures, sous forme de produit jetable, possédant une épaisseur de 3 mm au plus et comportant une couche de non-tissé absorbant les liquides avec ou à base de fibre de cellulose, caractérisée en ce que la semelle est formée par une seule couche de voile d'ouate (4) en fibre de cellulose possédant au moins 25% en poids de fibres de liage thermofusibles, laquelle couche est consolidée par gaufrage par calandrage et présente des zones gaufrées hautement compactées (9) et des zones au contraire moins compactées (10).
- Semelle orthopédique selon la revendication 1, caractérisée en ce que son épaisseur est comprise entre 1 et 3 mm, en particulier entre 1 et 2 mm.
- Semelle orthopédique selon la revendication 1, caractérisée en ce que sa densité est comprise entre 0,1 et 0,5 g/cm3, en particulier entre 0,2 et 0,3 g/cm3.
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce que les zones gaufrées hautement compactées (9) représentent une part comprise entre 8 et 20% de la surface de la couche de voile d'ouate (4).
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce que les zones gaufrées hautement compactées (9) présentent une profondeur d'au moins 0,5 mm et une dimension la plus courte dans le plan comprise entre 0,3 et 0,6 mm.
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce que la force maximale de traction de la bande de voile d'ouate (4) à l'état sec est comprise entre 35 et 100 N/25 mm dans le sens longitudinal et entre 40 et 100 N/25 mm dans le sens transversal.
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce que la force maximale de traction de la bande de voile d'ouate (4) à l'état humide est comprise entre 20 et 100 N/25 mm dans le sens longitudinal et entre 30 et 80 N/25 mm dans le sens transversal.
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce qu'elle présente une capacité d'absorption d'eau de 1 à 4 g de liquide par g de la couche de voile d'ouate.
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce qu'elle présente une résistance interne > 170 N/25 cm2, de préférence > 180 N/25 cm2.
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce que la couche de voile d'ouate (4) contient des fibres de coton.
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce que les fibres de liage thermofusibles, en particulier des fibres multi-composants, présentent du polyéthylène (PE) et/ou du polypropylène (PP) et/ou du polyester (PES).
- Semelle orthopédique selon l'une des revendications précédentes, caractérisée en ce qu'il est prévu, sur la face inférieure (12) de la semelle orthopédique (2) orientée en utilisation vers la semelle intérieure d'une chaussure, un dispositif antidérapant (14) en forme d'îlots ou de lignes.
- Semelle orthopédique selon la revendication 12, caractérisée en ce que le dispositif antidérapant (14) présente une dimension la plus grande de 1,5 mm au plus, en particulier de 1 mm au plus.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10235511A DE10235511A1 (de) | 2002-07-29 | 2002-07-29 | Einlegesohle |
| DE10235511 | 2002-07-29 | ||
| PCT/EP2003/008217 WO2004012549A1 (fr) | 2002-07-29 | 2003-07-25 | Semelle |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1524925A1 EP1524925A1 (fr) | 2005-04-27 |
| EP1524925B1 true EP1524925B1 (fr) | 2008-08-20 |
Family
ID=30128688
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP03766298A Expired - Lifetime EP1524925B1 (fr) | 2002-07-29 | 2003-07-25 | Semelle |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US20060035061A1 (fr) |
| EP (1) | EP1524925B1 (fr) |
| JP (1) | JP4490814B2 (fr) |
| AT (1) | ATE405186T1 (fr) |
| AU (1) | AU2003250178A1 (fr) |
| DE (2) | DE10235511A1 (fr) |
| WO (1) | WO2004012549A1 (fr) |
Families Citing this family (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1629738A1 (fr) | 2004-08-26 | 2006-03-01 | Solveig Kesby | Premières ou inserts pour chaussures absorbant la sueur et l'odeur |
| DE102007046273A1 (de) | 2007-09-20 | 2009-07-30 | Klaus Sommer | Voluminöse, mehrschichtige Einlegesohle |
| CN103158416A (zh) * | 2011-12-15 | 2013-06-19 | 吴聪裕 | 皮/革制品的真空吸塑加工方法 |
| ES2879615T3 (es) * | 2015-09-17 | 2021-11-22 | Cmc Consumer Medical Care Gmbh | Plantilla |
| DE102016109595A1 (de) * | 2016-05-24 | 2017-11-30 | Cmc Consumer Medical Care Gmbh | Einlegesohle |
| US20190269196A1 (en) * | 2018-03-01 | 2019-09-05 | Anthony Jason Riddick | FootPrnts |
| JP7461750B2 (ja) * | 2020-01-31 | 2024-04-04 | 白元アース株式会社 | 靴用中敷き |
| CH717440A2 (de) * | 2020-05-18 | 2021-11-30 | Flawa Consumer Gmbh | Grössenanpassbare Einlegesohle. |
Family Cites Families (23)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1831936U (de) * | 1960-12-20 | 1961-05-25 | Horst Brotzki | Einlegesohle. |
| US3148463A (en) * | 1962-10-18 | 1964-09-15 | Douglas G Tibbitts Jr | Disposable tissue sock |
| DE1886838U (de) * | 1963-11-07 | 1964-01-30 | Eva Zorn | Hygienische schuheinlage. |
| US3852897A (en) * | 1968-07-23 | 1974-12-10 | F Bridge | Footwear |
| US4062131A (en) * | 1976-09-10 | 1977-12-13 | Scholl, Inc. | Insoles for footwear |
| DE2728774C3 (de) * | 1977-06-25 | 1980-04-10 | Deutsche Gold- Und Silber-Scheideanstalt Vormals Roessler, 6000 Frankfurt | Schuhinnenmaterial, wie Brandsohlen- und Zwischensohlenmaterial, in Bahnform oder in Zuschnitten daraus |
| EP0033448A1 (fr) * | 1980-01-18 | 1981-08-12 | Ag Depharma | Protection de pied |
| US4610743A (en) * | 1980-08-29 | 1986-09-09 | James River-Norwalk, Inc. | Pattern bonding and creping of fibrous substrates to form laminated products |
| DE3215526A1 (de) * | 1982-04-26 | 1983-12-22 | geb. Sebesta Alenka Antonie 8500 Nürnberg Peters | Hygienische schuheinlegesohle |
| JPS6099201A (ja) * | 1983-11-05 | 1985-06-03 | 小松精練株式会社 | 抗菌性覆物材料 |
| JPS60212101A (ja) * | 1984-04-05 | 1985-10-24 | 株式会社クラレ | 靴部材およびその製造法 |
| DE3442502A1 (de) * | 1984-11-22 | 1986-05-22 | Nitex GmbH, 3002 Wedemark | Einlegesohle |
| CH669892A5 (fr) * | 1985-08-08 | 1989-04-28 | Flawa Schweiz Verband Wattefab | |
| JPS6279004A (ja) * | 1985-09-30 | 1987-04-11 | 株式会社クラレ | 靴中敷材 |
| US4864740A (en) * | 1986-12-22 | 1989-09-12 | Kimberly-Clark Corporation | Disposable hygienic shoe insole and method for making the same |
| JPS6464602A (en) * | 1987-09-04 | 1989-03-10 | Mitsubishi Petrochemical Co | Inner sole for shoes |
| CH679442A5 (fr) * | 1989-08-14 | 1992-02-28 | Flawa Schweiz Verband Wattefab | |
| JP3016166B2 (ja) * | 1991-09-06 | 2000-03-06 | 株式会社アシックス | エンボスシート並びにその製造方法並びにこれを使用した靴底 |
| JP2515473Y2 (ja) * | 1992-06-23 | 1996-10-30 | 株式会社クラレ | 靴の内張材 |
| JPH09308A (ja) * | 1995-06-22 | 1997-01-07 | Toyobo Co Ltd | 靴用下敷材 |
| DE19525858C1 (de) * | 1995-07-15 | 1996-11-14 | Freudenberg Carl Fa | Einlegesohle für Schuhe und Verfahren zur Herstellung |
| JPH11187905A (ja) * | 1997-12-26 | 1999-07-13 | Kochi Prefecture | 靴中敷 |
| DE29800474U1 (de) * | 1998-01-13 | 1998-04-09 | Schiele & Hirsch GmbH, 85116 Egweil | Lage aus einem Faser-Wirkstoff-Gemisch |
-
2002
- 2002-07-29 DE DE10235511A patent/DE10235511A1/de not_active Withdrawn
-
2003
- 2003-07-25 AT AT03766298T patent/ATE405186T1/de not_active IP Right Cessation
- 2003-07-25 WO PCT/EP2003/008217 patent/WO2004012549A1/fr not_active Ceased
- 2003-07-25 DE DE50310375T patent/DE50310375D1/de not_active Expired - Lifetime
- 2003-07-25 US US10/522,411 patent/US20060035061A1/en not_active Abandoned
- 2003-07-25 JP JP2004525318A patent/JP4490814B2/ja not_active Expired - Fee Related
- 2003-07-25 AU AU2003250178A patent/AU2003250178A1/en not_active Abandoned
- 2003-07-25 EP EP03766298A patent/EP1524925B1/fr not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| WO2004012549A1 (fr) | 2004-02-12 |
| AU2003250178A1 (en) | 2004-02-23 |
| JP2005534386A (ja) | 2005-11-17 |
| JP4490814B2 (ja) | 2010-06-30 |
| US20060035061A1 (en) | 2006-02-16 |
| EP1524925A1 (fr) | 2005-04-27 |
| DE50310375D1 (de) | 2008-10-02 |
| ATE405186T1 (de) | 2008-09-15 |
| DE10235511A1 (de) | 2004-02-12 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69820611T2 (de) | Dreidimensionale strukturen zum gebrauch als waschtücher | |
| EP1521879B1 (fr) | Rondelle cosmetique et procede de fabrication de ladite rondelle | |
| DE60033033T2 (de) | Absorbierende und schnittfeste mehrzweckfolienmaterialien | |
| DE2800132C2 (de) | Schmiegsamer Hautreinigungsartikel | |
| DE2934009A1 (de) | Gepraegter mob mit gepraegtem reinigungselement aus nichtgewebtem bahnmaterial | |
| EP0414634B1 (fr) | Insertion de chaussure et procédé de fabrication de celle-ci | |
| DE2723141A1 (de) | Wegwerfhandtuch, insbesondere zur verwendung fuer medizinische zwecke, und verfahren zu seiner herstellung | |
| DE2460712B2 (de) | Absorptionsvortage und Verfahren zu deren Herstellung | |
| WO1999025281A1 (fr) | Procede et dispositif pour produire une bande de materiau fibreux a base de fibres de cellulose, s'utilisant dans le domaine des articles d'hygiene | |
| DE1635231A1 (de) | Verfahren zur Verformung einer Bahn eines fasrigen Textilmaterials | |
| DE1965716B2 (de) | Saugfähige Bahn aus Zellulosefasern und Verfahren zu deren Herstellung | |
| DE2047439A1 (de) | Wegwerfwindel | |
| EP3462957B1 (fr) | Semelle intérieure | |
| DE69509879T2 (de) | Wegwerfhautreinigungsgegenstände | |
| DE10235511A1 (de) | Einlegesohle | |
| EP0555178B1 (fr) | Article flexible | |
| EP3360993B1 (fr) | Tapis de protection de surface absorbant jetable | |
| DE10361339B4 (de) | Kosmetisches Wattepad und Verfahren zum Herstellen eines kosmetischen Wattepads | |
| EP4054394B1 (fr) | Lingette pour le nettoyage et la désinfection d'objets et de surfaces | |
| DE3009585C2 (de) | Reinigungstuch | |
| WO2018158351A1 (fr) | Semelle intérieure | |
| EP1630276B1 (fr) | pad en cotton | |
| EP1676558B1 (fr) | Tampon cosmétique | |
| DE102020117127A1 (de) | Wischtuch für die Reinigung und Desinfektion von Gegenständen und Oberflächen | |
| DE102020120291A1 (de) | Reinigungstuch mit einem absorbierenden Vliesmaterial sowie Verfahren zur Herstellung |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20041207 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK |
|
| DAX | Request for extension of the european patent (deleted) | ||
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: ROEMPP, ANGELA Inventor name: MANGOLD, RAINER Inventor name: MICHELMANN, JANA |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: MICHELMANN, JANA Inventor name: MANGOLD, RAINER Inventor name: ROEMPP, ANGELA |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50310375 Country of ref document: DE Date of ref document: 20081002 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081201 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081120 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090120 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20090525 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081120 |
|
| BERE | Be: lapsed |
Owner name: PAUL HARTMANN A.G. Effective date: 20090731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090731 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090731 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081121 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090725 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090725 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090221 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080820 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20160722 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20160722 Year of fee payment: 14 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20170725 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20180330 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170725 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170731 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20210721 Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50310375 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230201 |