EP1114776B1 - Verfahren und Vorrichtung zum Verpacken von flachen Gegenständen - Google Patents
Verfahren und Vorrichtung zum Verpacken von flachen Gegenständen Download PDFInfo
- Publication number
- EP1114776B1 EP1114776B1 EP00126768A EP00126768A EP1114776B1 EP 1114776 B1 EP1114776 B1 EP 1114776B1 EP 00126768 A EP00126768 A EP 00126768A EP 00126768 A EP00126768 A EP 00126768A EP 1114776 B1 EP1114776 B1 EP 1114776B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- packaging
- packaging station
- station
- blank
- objects
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004806 packaging method and process Methods 0.000 title claims abstract description 59
- 238000000034 method Methods 0.000 title claims abstract description 13
- 238000007599 discharging Methods 0.000 abstract 1
- 238000012856 packing Methods 0.000 description 5
- 238000010586 diagram Methods 0.000 description 2
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B5/00—Packaging individual articles in containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, jars
- B65B5/02—Machines characterised by incorporation of means for making the containers or receptacles
- B65B5/024—Machines characterised by incorporation of means for making the containers or receptacles for making containers from preformed blanks
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B25/00—Packaging other articles presenting special problems
- B65B25/14—Packaging paper or like sheets, envelopes, or newspapers, in flat, folded, or rolled form
Definitions
- the invention relates to a method for packaging flat, stacked objects, especially of envelopes, packaging bags and the like, as described in the preamble of claim 1.
- Such a method is known for packaging frames from FR 2 285 301.
- the frame stacks are each made using two blanks, a box blank and a lid blank, packed. This is the first processing position a stack of box blanks and the second processing position assigned a stack of lid blanks, each with a box blank inserted under the transversely moving stack and a lid blank in each is advanced one position above the already nested stack.
- This known method works like other known methods for Packing stacked envelopes for example according to WO 96/20869 in a satisfactory manner Wise. Nevertheless, the invention is based on the object Process to be designed so that both the number of packaged per unit time Objects can be increased and the process with a device can be performed that takes up as little space as possible.
- the invention provides that the objects as a stack and the packaging blanks on their way to the packaging station initially towards each other and offset parallel to each other that the flat objects are then moved to reach the packaging station perpendicular to its original transport direction transported and then on a packaging blank be dropped off; be discontinued; be deducted; be dismissed. Thereupon the stacked items at two processing positions of the packaging station packed in the packaging blank to form a package, whereupon the package transversely to the original transport direction of the Objects are removed from the packing station. The The next packaging cut is always made using the the package containing the packed items over or over the second processing position beyond the first processing position fed to the packing station.
- the use of two processing positions in the packaging station leads to an increase in the number of items, that can be packed per unit of time.
- the next one Stack can already be placed on a packaging blank, if the previous stack is not completely in its Package is packed.
- the supply of the packaging station with new packaging cuts takes place via the second processing position or over the last completed package. This is one particularly space and space-saving arrangement of the various Components of the device possible.
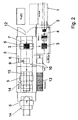
- Items 2 such as envelopes and the like will be first stacked and then as stack 3 across their original Transport direction 4 moves and on a packaging blank 5 deposited in a packaging station 6.
- the packing station 6 has two processing positions 7 and 8, the stack 3 in the first processing position 7 partially packed in the packaging blank 5 and in the second processing position 8 for example by hanging up and closing a cover part 9 is completely packed as a package 10.
- This Package 10 is then again transverse to the original direction of transport 4 in the direction of arrow 11 in Fig. 1 from the packaging station 6 discharged and leaves the device 12 for Example of a roller conveyor 13.
- the stack 14 is optionally raised completely, whereupon the top packaging blank 5 in each case over the processing position 8 or over a package 10 located there transported to processing position 7 and there on a Document is lowered.
- processing position 7 takes the packaging blank 5 a layer such that the objects 2 existing stacks 3 pushed onto or onto it can be removed.
- 1 shows the packaging blank 5 in a position already partially surrounding the stack 3.
- the stack 3 is not only on the Bottom of the packaging blank 5 placed exactly, but there are also the side flaps of the packaging blank 5 folded on the stack 3 and fixed.
- the packaging is therefore in position 7 except for the lid.
- the partially packed stack becomes processing position 7 3 then moved to the processing position 8 and there or on the way there the cover part 9 is brought into the closed position. It is also conveniently fixed there. Finally the packaged stack 3 becomes package 10 from the second processing position 8 of the packing station 6 ejected.
- the direction of movement of the blanks 5 and the objects 2 is initially done towards each other and offset in parallel to each other.
- the blanks 5 are from an original Stack height raised first, then over the processing position 8 horizontally up to the processing position 7 moved and lowered there to the level of the stack 3.
- the partially packaged stack 3 moves out of the processing position 7 in the processing position 8 parallel to the direction of movement the packaging blanks 5 that are horizontally above the processing position 8 are fed to the processing position 7.
- the completed package 10 is transverse to the direction of movement from processing position 7 to processing position 8 moving, partially completed package from the packaging station 6 removed.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Packaging Of Special Articles (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Container Filling Or Packaging Operations (AREA)
- Wrapping Of Specific Fragile Articles (AREA)
- Supplying Of Containers To The Packaging Station (AREA)
Description
- Fig. 1:
- eine Prinzipskizze des Verfahrens und
- Fig. 2:
- eine Draufsicht auf die Vorrichtung
Claims (3)
- Verfahren zum Verpacken von flachen, gestapelten Gegenständen (2), insbesondere von Briefhüllen, Verpackungsbeuteln und dergleichen, bei dem zunächst die aus einer Produktionsmaschine (1) kommenden flachen Gegenstände (2) gestapelt und sodann in einer Verpackungsstation (6) zumindest teilweise unter Verwendung von mindestens einem Verpackungszuschnitt (5) verpackt und daraufhin weitertransportiert und aus der Verpackungsstation (6) ausgeschleust werden, wobeia) die gestapelten Gegenstände (2) und die Verpackungszuschnitte (5) zum Erreichen der Verpackungsstation (6) zunächst aufeinanderzub) sowie parallel versetzt zueinander bewegt werden,c) die aus den Gegenständen (2) bestehenden Stapel (3) zum Erreichen der Verpackungsstation (6) quer zur ursprünglichen Transportrichtung (4) der Gegenstände (2) bewegt und in der Verpackungsstation (6) auf einen Verpackungszuschnitt (5) abgesetzt werden,d) die Stapel (3) in zwei Verarbeitungspositionen (7, 8) der Verpackungsstation (6) in Verpackungszuschnitte (5) verpackt werden unde) als Pakete (10) quer zur ursprünglichen Transportrichtung (4) der Gegenstände (2) aus der Verpackungsstation (6) ausgeschleust werden,
dadurch gekennzeichnet,f) dass der jeweils nächste Verpackungszuschnitt (5) über das die verpackten Gegenstände (2) enthaltende Paket (10) bzw. über die zweite Verarbeitungsposition (8) hinweg der ersten Verarbeitungsposition (7) der Verpackungsstation (6) zugeführt wird. - Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass die Stapel (3) in der ersten Verarbeitungsposition (7) in den Verpackungszuschnitt (5) dadurch teilweise verpackt werden, dass die Seitenklappen an den Stapel (3) heran geklappt und fixiert werden.
- Verfahren nach Anspruch 1oder 2, dadurch gekennzeichnet, dass mindestens ein als Deckelteil (9) dienendes Teil des Verpackungszuschnittes (5) in der zweiten Verarbeitungsposition (8) auf dem teilweise fertiggestellten Paket (10) in die Schließlage gebracht und gegebenenfalls fixiert wird.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19962302A DE19962302A1 (de) | 1999-12-23 | 1999-12-23 | Verfahren und Vorrichtung zum Verpacken von flachen Gegenständen |
| DE19962302 | 1999-12-23 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1114776A2 EP1114776A2 (de) | 2001-07-11 |
| EP1114776A3 EP1114776A3 (de) | 2001-09-05 |
| EP1114776B1 true EP1114776B1 (de) | 2004-08-18 |
Family
ID=7934008
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP00126768A Expired - Lifetime EP1114776B1 (de) | 1999-12-23 | 2000-12-06 | Verfahren und Vorrichtung zum Verpacken von flachen Gegenständen |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US6591587B2 (de) |
| EP (1) | EP1114776B1 (de) |
| JP (1) | JP2001219912A (de) |
| AT (1) | ATE273839T1 (de) |
| DE (2) | DE19962302A1 (de) |
| NO (1) | NO321630B1 (de) |
Families Citing this family (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10123356A1 (de) * | 2001-05-14 | 2002-11-28 | Ligmatech Automationssysteme | Verpackungsvorrichtung |
| US7398134B2 (en) * | 2004-09-01 | 2008-07-08 | Hallmark Cards, Incorporated | Sorting apparatus with arbitrary user-specified sequence control |
| DE102005045864B4 (de) * | 2005-09-21 | 2007-05-10 | Daniel Calandri | Verpackungsanlage und Verpackungsverfahren |
| EP1790603B1 (de) * | 2005-11-23 | 2010-01-20 | Müller Martini Holding AG | Verfahren und Einrichtung zum Zwischenlagern von Stapeln |
| US7316103B2 (en) * | 2006-06-05 | 2008-01-08 | Graphic Packaging International, Inc. | Continuous motion packaging system |
| US7703196B2 (en) * | 2006-07-13 | 2010-04-27 | John Mezzalingua Associates, Inc. | Compression tool length adjuster |
| US7584589B2 (en) * | 2007-03-09 | 2009-09-08 | Georgia-Pacific Consumer Products Lp | Robotic multi-product case-packing system |
| US8777093B2 (en) * | 2008-04-29 | 2014-07-15 | Rock-Tenn Shared Services, Llc | Polygonal container and blank for making the same |
| US9994352B2 (en) | 2008-04-29 | 2018-06-12 | Westrock Shared Services, Llc | Polygonal container and blank for making the same |
| DE102008029766B4 (de) * | 2008-06-25 | 2013-04-04 | Winkler + Dünnebier Gmbh | Vorrichtung zum Verpacken von flachen Artikeln |
| KR101184450B1 (ko) * | 2010-10-05 | 2012-09-20 | 삼성전자주식회사 | 자동포장장치 및 자동포장방법 |
| CN105151353B (zh) * | 2015-08-17 | 2017-06-16 | 泉州市合能工业机器人有限公司 | 一种全自动智能捡砖装箱系统 |
| DE102016221887B4 (de) * | 2016-11-08 | 2018-07-12 | SOMIC Verpackungsmaschinen GmbH & Co. KG | Verpackungsanlage |
| CN109353835B (zh) * | 2018-12-21 | 2023-10-13 | 江苏江桥机械制造有限公司 | 一种自动高速砌块码垛生产线 |
Family Cites Families (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| NL6816267A (de) * | 1968-11-15 | 1970-05-20 | ||
| US3832826A (en) * | 1970-05-21 | 1974-09-03 | Huntingdon Ind Inc | Box forming and filling method and machine |
| DE2123991A1 (de) * | 1971-02-04 | 1972-08-17 | Canadian International Paper Co., Montreal, Quebec (Kanada) | Verpackungsmaschine |
| US3986319A (en) * | 1973-02-20 | 1976-10-19 | Emhart Industries, Inc. | Wrap-around packer |
| FR2285301A1 (fr) * | 1974-09-17 | 1976-04-16 | Surepack | Machine pour l'empaquetage et l'emballage automatique de ramettes |
| DE3400822A1 (de) * | 1984-01-12 | 1985-07-25 | Inmarco AG, Oberurnen | Verfahren zum verpacken von warengruppen in einer faltschachtel sowie vorrichtung zur durchfuehrung des verfahrens |
| CH663185A5 (de) * | 1984-05-09 | 1987-11-30 | Sig Schweiz Industrieges | Vorrichtung zum selbsttaetigen einfuellen von gestapelten, scheibenfoermigen gegenstaenden in einseitig offene verpackungsbehaelter. |
| US4660352A (en) * | 1985-12-23 | 1987-04-28 | Package Machinery Company | Apparatus and method for packaging compressible pouches |
| FR2687634B1 (fr) * | 1992-02-20 | 1994-05-13 | Otor | Procede et flan pour la realisation d'une caisse autour d'une charge, et caisse ainsi obtenue. |
| JPH08119239A (ja) * | 1994-10-31 | 1996-05-14 | Sony Corp | カートン処理システム及びカートン処理方法 |
| IT1273839B (it) * | 1994-11-11 | 1997-07-11 | Azionaria Costruzioni Acma Spa | Metodo e macchina di incarto per gruppi di prodotti |
| FI97355C (fi) * | 1995-01-04 | 1996-12-10 | Jopamac Ab Oy | Laitteisto pinkassa olevan paperitavaran pakkaamiseksi |
| SE9601784D0 (sv) * | 1996-05-08 | 1996-05-08 | Rieber & Soen As | Behållare, särskilt ask för påsar, samt anordning för framställning, i synnerhet fyllning och tillslutning av sådana behållare |
| FI101954B1 (fi) * | 1996-09-27 | 1998-09-30 | Jomet Oy | Menetelmä ja laitteisto litteiden esineiden pakkaamiseksi |
| DE19834024A1 (de) * | 1998-07-28 | 2000-02-03 | Focke & Co | (Tray-)Packung für eine Gruppe von Gegenständen sowie Verfahren und Vorrichtung zum Herstellen derselben |
| IT1304400B1 (it) * | 1998-10-13 | 2001-03-19 | Azionaria Costruzioni Acma Spa | Metodo e macchina per l'incarto di un prodotto. |
-
1999
- 1999-12-23 DE DE19962302A patent/DE19962302A1/de not_active Withdrawn
-
2000
- 2000-12-06 EP EP00126768A patent/EP1114776B1/de not_active Expired - Lifetime
- 2000-12-06 DE DE50007465T patent/DE50007465D1/de not_active Expired - Lifetime
- 2000-12-06 AT AT00126768T patent/ATE273839T1/de not_active IP Right Cessation
- 2000-12-15 US US09/738,221 patent/US6591587B2/en not_active Expired - Fee Related
- 2000-12-19 NO NO20006476A patent/NO321630B1/no unknown
- 2000-12-25 JP JP2000392806A patent/JP2001219912A/ja active Pending
Also Published As
| Publication number | Publication date |
|---|---|
| NO321630B1 (no) | 2006-06-12 |
| DE50007465D1 (de) | 2004-09-23 |
| EP1114776A3 (de) | 2001-09-05 |
| ATE273839T1 (de) | 2004-09-15 |
| JP2001219912A (ja) | 2001-08-14 |
| NO20006476L (no) | 2001-06-25 |
| EP1114776A2 (de) | 2001-07-11 |
| NO20006476D0 (no) | 2000-12-19 |
| US20010005972A1 (en) | 2001-07-05 |
| DE19962302A1 (de) | 2001-09-06 |
| US6591587B2 (en) | 2003-07-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0421148B1 (de) | Verfahren und Vorrichtung zum Transport von Stapeln von Zuschnitten für die Herstellung von (Zigaretten-)Packungen | |
| EP3012197B1 (de) | Vorrichtung und verfahren zum umgang mit artikeln | |
| DE602004001846T2 (de) | Vorrichtung und Verfahren zur Verpackung und Palletieren von Toiletten- und/oder Küchenpapierrollen | |
| DE68906281T2 (de) | Verfahren zum Entleeren einer zusammendrückbaren Ladung einer Vielzahl von Artikeln aus einem Behälter und Apparat zur Ausführung des Verfahrens. | |
| CH716125B1 (de) | Vorrichtung und Verfahren zum Depalettieren von gestapelten Stückgutgebinden. | |
| DE69604380T2 (de) | Verpackungsvorrichtung für aufgestapelte papiererzeugnisse | |
| EP3372516B1 (de) | Verpackungsvorrichtung und verfahren zum aufsetzen einzelner artikel oder zusammenstellungen an artikeln auf flächige verpackungszuschnitte | |
| DE1955937A1 (de) | Verfahren und Vorrichtung zum Sortieren und Verpacken von Artikeln in einen Behaelter | |
| DE102019113129B4 (de) | Verpackungsmaschine zum anordnen von elementen, vorzugsweise kartons, auf paletten, und verfahren hierfür | |
| EP0653354B1 (de) | Verpackung für Bücher und/oder andere Produkte sowie Verfahren und Vorrichtung zu ihrer Herstellung | |
| EP1114776A2 (de) | Verfahren und Vorrichtung zum Verpacken von flachen Gegenständen | |
| EP3303153B1 (de) | Verfahren und vorrichtung zum zuführen von produkten in behälter | |
| DE102018132242A1 (de) | Vorrichtung und Verfahren zur schichtweisen Handhabung von übereinander angeordneten Stückgutlagen | |
| DE102018203180A1 (de) | Verpackungsvorrichtung für Artikel und Verfahren zum Verpacken von Artikeln | |
| EP3109018B1 (de) | Tiefziehverpackungsmaschine mit komplettschnittstation und entsprechendes verfahren | |
| DE2838580A1 (de) | Verfahren zum verpacken von verformbaren produkten, z.b. biegsamen beuteln, in behaeltern und vorrichtung zur durchfuehrung dieses verfahrens | |
| EP3312099B1 (de) | Verfahren zum herstellen einer palettenlosen verpackungseinheit und nach dem verfahren hergestellte verpackungseinheit | |
| EP2537766B1 (de) | Komplettschnittstation und Verfahren zum Vereinzeln von Verpackungen | |
| DE102006003338A1 (de) | Gebinde sowie Verfahren und Vorrichtung zum Herstellen eines Gebindes | |
| EP4112486A1 (de) | Verpackungsmagazin für einen manipulator und verpackungssystem zum herstellen von gebinden | |
| DE2636320C2 (de) | Vorrichtung zum automatischen Palettieren von Gegenständen, insbesondere Flaschen | |
| EP1864923A1 (de) | Verfahren und Vorrichtung zur Stapelung und Palettierung von Transportbehältern | |
| DE19736730A1 (de) | Gebindepackung für Zigaretten sowie Verfahren und Vorrichtung zum Herstellen derselben | |
| DE102017102913A1 (de) | Vorrichtung und Verfahren zur flexiblen Verteilung von Verpackungen | |
| EP2119650B1 (de) | Verfahren und Vorrichtung zur Palettierung von Stückgut |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20020119 |
|
| AKX | Designation fees paid |
Free format text: AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| 17Q | First examination report despatched |
Effective date: 20030404 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20040818 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040818 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040818 Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040818 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040818 Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040818 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040818 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50007465 Country of ref document: DE Date of ref document: 20040923 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041118 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041118 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041118 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041206 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041206 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041231 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041231 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041231 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041231 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20040818 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| BERE | Be: lapsed |
Owner name: WINKLER + DUNNEBIER A.G. Effective date: 20041231 |
|
| 26N | No opposition filed |
Effective date: 20050519 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| EN | Fr: translation not filed | ||
| BERE | Be: lapsed |
Owner name: *WINKLER + DUNNEBIER A.G. Effective date: 20041231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050118 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20101220 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20110218 Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 50007465 Country of ref document: DE Owner name: WINKLER + DUENNEBIER GMBH, DE Free format text: FORMER OWNER: WINKLER+DUENNEBIER AG, 56564 NEUWIED, DE Effective date: 20120327 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111206 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50007465 Country of ref document: DE Effective date: 20120703 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120703 |