EP0067398B1 - Hohlgeschirr-Giessvorrichtung - Google Patents
Hohlgeschirr-Giessvorrichtung Download PDFInfo
- Publication number
- EP0067398B1 EP0067398B1 EP82104986A EP82104986A EP0067398B1 EP 0067398 B1 EP0067398 B1 EP 0067398B1 EP 82104986 A EP82104986 A EP 82104986A EP 82104986 A EP82104986 A EP 82104986A EP 0067398 B1 EP0067398 B1 EP 0067398B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- gripping
- another
- mould unit
- application surfaces
- mould
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
- 238000000465 moulding Methods 0.000 title 1
- 238000005266 casting Methods 0.000 claims abstract description 13
- 230000007246 mechanism Effects 0.000 claims abstract 10
- 238000006073 displacement reaction Methods 0.000 description 2
- 238000009434 installation Methods 0.000 description 2
- 238000005267 amalgamation Methods 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000000919 ceramic Substances 0.000 description 1
- 239000006063 cullet Substances 0.000 description 1
- 229910052571 earthenware Inorganic materials 0.000 description 1
- 230000002452 interceptive effect Effects 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 239000011505 plaster Substances 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B1/00—Producing shaped prefabricated articles from the material
- B28B1/26—Producing shaped prefabricated articles from the material by slip-casting, i.e. by casting a suspension or dispersion of the material in a liquid-absorbent or porous mould, the liquid being allowed to soak into or pass through the walls of the mould; Moulds therefor ; specially for manufacturing articles starting from a ceramic slip; Moulds therefor
- B28B1/265—Producing shaped prefabricated articles from the material by slip-casting, i.e. by casting a suspension or dispersion of the material in a liquid-absorbent or porous mould, the liquid being allowed to soak into or pass through the walls of the mould; Moulds therefor ; specially for manufacturing articles starting from a ceramic slip; Moulds therefor pressure being applied on the slip in the filled mould or on the moulded article in the mould, e.g. pneumatically, by compressing slip in a closed mould
- B28B1/266—Means for counteracting the pressure being applied on the slip or on the moulded article in the mould, e.g. means for clamping the moulds parts together in a frame-like structure
Definitions
- the invention relates to a hollow crockery casting device comprising a mold unit having one or more individual molds arranged in a row, which is divided into two halves along the row of individual molds, and a gripping device with two gripping members which can be pressed against one another and which hold the mold unit on two mutually opposite sides in a manner that presses the two halves of the mold unit against each other.
- the dividing line runs between the opposite sides of the mold unit which are gripped by the gripping members, that is to say transversely to the direction of pressure of the gripping members. In this way, when gripping the mold unit, the pressure of a mold unit filled with slip is also counteracted, which tries to push the two mold halves apart.
- the known procedure has the disadvantage that either several closely-fitting mold units must be gripped simultaneously with a single gripping device, or the distance between the individual mold units which are brought to the gripping device on a conveyor belt extending transversely to the transport direction is at least correspondingly the space required for a gripping element, including its linear displacement, must be selected.
- the invention is based on the object of demonstrating a way in which as many mold units, which may contain different individual molds in each case, can be processed per unit time in a hollow tableware casting installation designed as a production line.
- a hollow tableware casting apparatus initially assumed to be known in that the dividing line of the mold unit runs from one to the opposite other side of the mold unit, each of which is gripped by a gripping member, on both sides of the dividing line on each side grasped by a gripping member to this inclined attack surfaces with opposing inclination are provided and that the gripping members each have a pair of preferably V-shaped extending towards the other gripping member away from each other for engagement with the engagement surfaces of the mold unit.
- the gripping members are effective in the direction of the dividing line.
- a mold unit when a mold unit is gripped, they still press their halves together, since they act in a wedge-like manner on surfaces inclined with respect to the dividing line, so that part of the force exerted by the gripping members is deflected transversely to the dividing line.
- Grasping a mold unit along the dividing line also allows the mold units to be arranged close to one another, transversely to the dividing lines, for example in the conveying direction of a belt.
- each mold unit can then be removed individually, so that it is possible to use different mold units which are different with regard to their individual shapes in such an overall system.
- the dense arrangement of the mold units allows maximum utilization of the conveying device of a hollow tableware casting device.
- the gripping device according to the invention can be used, for example, in transfer and transfer stations of cave caster casting systems, where the mold is to be placed on a conveyor belt on another conveyor belt, or in the pouring station, in which the mold unit is gripped and after 180 ° for pouring out the residual schikker the cullet formation is rotated.
- the oblique engagement surfaces for the gripping elements are preferably provided at the corners of the otherwise essentially rectangular mold unit.
- the angle which the oblique contact surfaces of a mold unit form with the dividing line is advantageously 45 ".
- the oblique engagement surfaces can also be curved, but a flat shape of the engagement surfaces is preferred.
- the gripping device is used in a pouring station, it is provided in a further embodiment of the invention that the gripping device is rotatably mounted about an axis running perpendicular to the line along which the gripping members press against one another.
- the mold unit 10 which will be referred to as a block mold in the following, consists of plaster. In the exemplary embodiment shown, it contains three individual shapes 10a, 10b and 10c, which are arranged in a straight line.
- the block shape 10 is along a dividing line 12, which runs through the center of the individual molds 10a, 10b and 10c, can be divided into two halves 10 'and 10 ". It should be noted that the outer sides of the bell mold 10 run essentially smoothly and in a straight line This overflow funnel, which is filled when the slip is poured in, has the task of compensating for the shrinkage which takes place when the slip dries on.
- the block molds 10 are each provided with a circumferential tensioning belt (not shown) in order to hold the two halves 10 ′, 10 ′′ together when they are conveyed on a conveyor belt (not shown) transversely to the dividing line 12.
- the gripping device has gripping members 16 ′, 16 ′′ which can be displaced relative to one another in the direction of the dividing line 12 of an advanced block mold 10, with gripping elements 18 ′, 18 ′, 18 ′′, 18 ′′ which extend away from one another in a V-shape.
- These gripping elements 18 ′, 18 ′ and 18 “, 18” engage on attack surfaces 20 ', 20' and 20 ", 20” which run obliquely to the dividing line 12 of the bell shape 10, as shown in FIG. 1.
- the block shape 10 is gripped and held together in an optimal manner, namely, forces arise from all directions from outside to inside.
- the block molds 10 can be arranged one behind the other transversely to the dividing line 12, without interfering with one another if they are to be gripped individually. This is due to the fact that due to the oblique course of the attack surfaces 20 ', 20' and 20 ", 20" in spite of the block molds 10 abutting against one another, there is a certain scope for the gripping elements 18 ', 18' and 18 ", 18" across the dividing line has been created.
- the block shapes 10 can also differ in their outer dimensions within a certain tolerance range, primarily in their width and length.
- the bearing 26 is fastened to a support rod 28 which is parallel to the guide rod 22 and which is vertical Guide rods 30 is slidable.
- the vertical guide rods 30 are slidably mounted on rollers 32 on rails 32 (see also FIG. 2).
- the gripping device can grasp a block shape, lift it, move it sideways, rotate it by 180 °, move it further and
- a movement sequence which can be achieved with the gripping device according to the invention, is of great advantage in the pouring station of a hollow tableware casting installation, where the block molds arriving on a conveyor belt are grasped, raised and laterally removed from the conveyor belt, then by 180 ° to pour out the slip and then shifted further sideways and upside down to the Abtro of the remaining slip are placed on a conveyor belt parallel to the first conveyor belt.
- the second conveyor belt runs in the opposite direction to the first conveyor belt.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Dispersion Chemistry (AREA)
- Manufacturing & Machinery (AREA)
- Mechanical Engineering (AREA)
- Specific Conveyance Elements (AREA)
- Manipulator (AREA)
- Moulds, Cores, Or Mandrels (AREA)
- Separation Using Semi-Permeable Membranes (AREA)
- Casting Devices For Molds (AREA)
Description
- Die Erfindung betrifft eine Hohlgeschirr-Gießvorrichtung mit einer eine oder mehrere in Reihe angeordnete Einzelformen aufweisenden Formeneinheit, die längs der Reihe der Einzelformen in zwei Hälften geteilt ist, und mit einer Greifeinrichtung mit zwei gegeneinander drückbaren Greiforganen, die die Formeneinheit auf zwei zueinander entgegengesetzten Seiten in einer die beiden Hälften der Formeneinheit gegeneinander drückenden Weise erfassen.
- Bei einer bekannten Hohlgeschirr-Gießvorrichtung dieser Art für Keramik, insbesondere Steingut, verläuft die Trennungslinie zwischen den von den Greiforganen erfaßten entgegengesetzten Seiten der Formeneinheit, also quer zur Druckrichtung der Greiforgane. Auf diese Weise wird beim Greifen der Formeneinheit auch dem Druck einer mit Schlicker gefüllten Formeneinheit entgegengewirkt, der die beiden Formhälften auseinanderzudrücken versucht.
- Das bekannte Vorgehen hat jedoch den Nachteil, daß entweder mehrere dicht an dicht anliegende Formeneinheiten gleichzeitig mit einer einzigen Greifeinrichtung erfaßt werden müssen oder aber der Abstand zwischen den einzelnen Formeneinheiten, die auf einem Transportband sich quer zur Transportrichtung erstreckend an die Greifeinrichtung herangeführt werden, mindestens entsprechend dem Raumbedarf eines Greiforgans einschließlich seiner linearen Verschiebung gewählt werden muß.
- Ein Zusammenschluß von mehreren Formeneinheiten zu einer Gesamtform mit einer Vielzahl von Reihen von Einzelformen nicht die Verwendung unterschiedlicher Einzelformen. Außerdem müßten die gegebenenfalls auf einem Förderband herantransportierten zu einer Gesamtform zusammengeschlossenen Formeneinheiten ebenfalls entsprechend der Größe der Greiforgane und deren Verschiebungsstrecke beabstandet sein.
- Der Erfindung liegt nun die Aufgabe zugrunde, einen Weg aufzuzeigen, wie möglichst viele Formeneinheiten, die gegebenenfalls jeweils unterschiedliche Einzelformen enthalten, pro Zeiteinheit in einer als Fertigungsstraße ausgebildeten Hohlgeschirr-Gießanlage bearbeitet werden können.
- Diese Aufgabe wird bei einer eingangs als bekannt vorausgesetzten Hohlgeschirr-Gießvorrichtung erfindungsgemäß dadurch gelöst, daß die Trennungslinie der Formeneinheit von der einen zu der entgegengesetzten anderen, jeweils von einem Greiforgan erfaßten Seite der Formeneinheit verläuft, daß an jeder von einem Greiforgan erfaßten Seite beidseits der Trennungslinie zu dieser schräg verlaufende Angriffsflächen mit einanderentgegengesetzter Neigung vorgesehen sind und daß die Greiforgane jeweils ein Paar vorzugsweise sich V-förmig in Richtung auf das andere Greiforgan voneinander weg erstreckende Greifelement für eine Anlage an die Angriffsflächen der Formeneinheit aufweisen.
- Gemäß der Erfindung sind also die Greiforgane in Richtung der Trennungslinie wirksam. Sie pressen aber trotzdem beim Ergreifen einer Formeneinheit deren Hälften zusammen, da sie keilartig an gegenüber der Trennungslinie geneigten Flächen angreifen, so daß ein Teil der von den Greiforganen ausgeübten Kraft quer zur Trennungslinie umgelenkt wird. Das Ergreifen einer Formeneinheit entlang der Trennungslinie erlaubt aber auch ein Anordnen der Formeneinheiten dicht an dicht quer zu den Trennungslinien, also beispielsweise in Förderrichtung eines Bandes. Trotz der dichten Anordnung der Formeneinheiten läßt sich aber jede Formeneinheit dann einzeln entnehmen, so daß es möglich ist, unterschiedliche Formeneinheiten, die unterschiedlich hinsichtlich ihrer Einzelformen sind, in einem derartigen Gesamtsystem zu verwenden. Die dichte Anordnung der Formeneinheiten erlaubt eine maximale Ausnutzung der Fördereinrichtung einer Hohlgeschirr-Gießvorrichtung.
- Die erfindungsgemäße Greifeinrichtung läßt sich beispielsweise in Umsetz- und Übersetzstationen von Höhlgeschirr-Gießanlagen verwenden, wo die Form von einem Förderband auf ein anderes Förderband gesetzt werden soll, oder in der Ausgießstation, in der die Formeneinheit erfaßt und um 180° zum Ausgießen des Restschlikkers nach der Scherbenausbildung gedreht wird.
- Vorzugsweise sind die schrägen Angriffsflächen für die Greifelemente an den Ecken der ansonsten im wesentlichen rechteckigen Formeneinheit vorgesehen.
- Der Winkel, den die schrägen Angriffsflächen einer Formeneinheit mit der Trennungslinie einschließen, beträgt vorteilhafterweise 45".
- Die schrägen Angriffsflächen können prinzipiell auch gekrümmt sein, jedoch wird eine ebene Form der Angriffsflächen bevorzugt.
- Wird die Greifeinrichtung in einer Ausgießstation verwendet, so ist in weiterer Ausbildung der Erfindung vorgesehen, daß die Greifeinrichtung um eine senkrecht zu der Linie, entlang welcher die Greiforgane gegeneinander drücken, verlaufende Achse drehbar gelagert ist.
- Weitere vorteilhafte Ausgestaltungen der Erfindung ergeben sich aus der nachstehenden, anhand der Zeichnung erfolgenden Beschreibung eines bevorzugten Ausführungsbeispiel. In der Zeichnung stellt dar
- Fig. 1 eine Draufsicht auf eine Greifeinrichtung und eine Formeneinheit gem. der Erfindung und
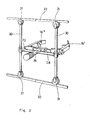
- Fig. 2 eine perspektivische Seitenansicht der Greifeinrichtung der Fig. 1 in einer Ausgießstation.
- Die Formeneinheit 10, die im Nachfolgenden kurz als Blockform bezeichnet wird, besteht aus Gips. Sie enthält in dem dargestellten Ausführungsbeispiel drei Einzelformen 10a, 10b und 10c, die in einer geradlinigen Reihe angeordnet sind. Die Blockform 10 ist entlang einerTrennungslinie 12, die mittig durch die Einzelformen 10a, 10b und 10c hindurchläuft, in zwei Hälften 10' und 10" teilbar. Zu bemerken ist, daß die Außenseiten der Glockform 10 im wesentlichen glatt und geradlinig verlaufen. Mit 14 ist ein Überlauftrichter bezeichnet, der den Einzelformen 10a, 10b und 10c zugeordnet ist, die auch über ihn miteinander in Verbindung stehen. Dieser Überlauftrichter, der beim Eingießen des Schlickers gefüllt wird, hat die Aufgabe, für einen Ausgleich der beim Antrocknen des Schlickers stattfindenden Schrumpfung zu sorgen.
- Ferner sind die Blockformen 10 jeweils mit einem (nicht gezeigten) umlaufenden Spannband versehen, um die beiden Hälften 10', 10" zusammenzuhalten, wenn sie auf einem (nicht gezeigten) Transportband quer zur Trennungslinie 12 herangefördert werden.
- Die Greifeinrichtung weist gegeneinander in Richtung der Trennungslinie 12 einer herangeführten Blockform 10 verschiebbare Greiforgane 16', 16" mit V-förmig voneinander weg sich streckenden Greifelementen 18', 18', 18", 18" auf. Diese Greifelemente 18', 18' und 18", 18" greifen an schräg zur Trennungslinie 12 der Glockform 10 verlaufenden Angriffsflächen 20', 20' und 20", 20" an, wie dies in Fig. 1 dargestellt ist. Die schrägen Angriffsflächen 20', 20' und 20", 20" entstehen durch Abschrägen der Ecken der ansonsten rechteckförmigen Blockform 10. Greifen nun die Greifelemente 18', 18' an den schrägen Angriffsflächen 20', 20' und die Greifelemente 18", 18" an den schrägen Angriffsflächen 20", 20" der Blockform 10 an, so wird die Blockform 10 in optimaler Weise ergriffen und zusammengehalten. Es treten dabei nämlich Kräfte aus allen Richtungen von außen nach innen auf.
- Wie man leicht aus Fig. 1 entnimmt, können die Blockformen 10 auf Stoß quer zur Trennungslinie 12 hintereinander angeordnet werden, ohne daß sie sich gegenseitig stören, wenn sie einzeln ergriffen werden sollen. Dies liegt daran, daß aufgrund des schrägen Verlaufs der Angriffsflächen 20', 20' und 20", 20" trotz der Anlage der Blockformen 10 auf Stoß ein gewisser Spielraum für die Greifelemente 18', 18' und 18", 18" quer zur Trennungslinie geschaffen worden ist.
- Ferner ist ohne weiteres aus Fig. 1 ersichtlich, daß die Blockformen 10 auch in ihren Außenabmessungen sich innerhalb eines gewissen Toleranzbereiches unterscheiden können, vornehmlich in ihrer Breite und in ihrer Länge. Der die Greifelemente 18', 18' bzw. 18", 18" verbindende Abschnitt der Greiforgane 16', 16" muß nämlich nicht in Anlage an die senkrecht zur Trennungslinie 12 verlaufenden Endflächen der Blockform 10 kommen.
- In diesem Zusammenhang sei auch bemerkt, daß es auch möglich ist, ohne sich vom Prinzip der Erfindung zu entfernen, anstelle der trapezartigen Endabschnitte der Blockform 10 eine gekrümmte, bogenförmige Ausbildung der Endabschnitte vorzusehen. Entsprechend würden dann die Greifelemente 18', 18' und 18", 18" verlaufen. Auch hier wird die in Richtung der Trennungslinie 12 wirkende Kraft zum Teil quer zur Trennungslinie umgelenkt.
- Die Greiforgane 16', 16" sind auf einer Führungsstange 22 verschiebbar, die quer zu einer Welle 24 befestigt ist, die ihrerseits in einem Lager 26 drehbar gelagert ist. Das Lager 26 ist an einer zur Führungsstange 22 parallelen Tragstange 28 befestigt, die in vertikalen Führungsstangen 30 verschiebbar ist. Die vertikalen Führungsstangen 30 sind über Rollen 31 an Schienen 32 verschiebbar gelagert (siehe auch Fig. 2). Auf diese Weise kann die Greifeinrichtung eine Blockform erfassen, anheben, seitlich verschieben, sich um 180° drehen, weiter verschieben und sie absetzen. Ein solcher. Bewegungsablauf, der mit der erfindungsgemäßen Greifeinrichtung erzielt werden kann, ist in der Ausgießstation einer Hohlgeschirr-Gießanlage von großem Vorteil, wo die auf einem Transportband ankommenden Blockformen erfaßt, angehoben und seitlich vom Transportband weggeführt werden, dann um 180° zum Ausgießen des Schlickers gedreht werden und dann weiter seitlich verschoben und auf dem Kopf stehend zum Abtropfen des Restschlickers auf ein zum ersten Förderband paralleles Förderband abgesetzt werden. Das zweite Förderband verläuft dabei in der entgegengesetzten Richtung wie das erste Förderband. Auf diese Weise wird das Ausgießen der Blockformen geschickt mit einem Umsetzen der Blockformen von einem Förderband auf ein anderes Förderband verbunden.
Claims (6)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT82104986T ATE10718T1 (de) | 1981-06-11 | 1982-06-08 | Hohlgeschirr-giessvorrichtung. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3123073A DE3123073C1 (de) | 1981-06-11 | 1981-06-11 | Vorrichtung fuer das Giessen von Hohlgeschirr |
| DE3123073 | 1981-06-11 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0067398A2 EP0067398A2 (de) | 1982-12-22 |
| EP0067398A3 EP0067398A3 (en) | 1983-08-17 |
| EP0067398B1 true EP0067398B1 (de) | 1984-12-12 |
Family
ID=6134392
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP82104986A Expired EP0067398B1 (de) | 1981-06-11 | 1982-06-08 | Hohlgeschirr-Giessvorrichtung |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0067398B1 (de) |
| AT (1) | ATE10718T1 (de) |
| DE (1) | DE3123073C1 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2253806A (en) * | 1991-02-27 | 1992-09-23 | Katsuji Takeno | Mould and positioning holder for mould |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3691266A (en) * | 1970-12-08 | 1972-09-12 | Regal China Corp | Supporting carriage for,and method of casting in,molds for the production of ceramic hollow ware |
| US4046272A (en) * | 1976-09-15 | 1977-09-06 | Hayward Donald J | Device for upending a ceramic mold |
-
1981
- 1981-06-11 DE DE3123073A patent/DE3123073C1/de not_active Expired
-
1982
- 1982-06-08 EP EP82104986A patent/EP0067398B1/de not_active Expired
- 1982-06-08 AT AT82104986T patent/ATE10718T1/de not_active IP Right Cessation
Also Published As
| Publication number | Publication date |
|---|---|
| EP0067398A2 (de) | 1982-12-22 |
| DE3123073C1 (de) | 1982-10-28 |
| ATE10718T1 (de) | 1984-12-15 |
| EP0067398A3 (en) | 1983-08-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3107584C2 (de) | ||
| DE69407213T2 (de) | Plattentrennmaschine | |
| DE2800407B2 (de) | Vorrichtung zum Greifen von im Zuge des Hersteilens von Steinen, insbesondere Kalksandsteinen, auf Lücke gepreßten bzw. angelieferten Steinformlingen | |
| DE2838739C2 (de) | Vorrichtung zum Schneiden von Ziegelformlingen aus einem Strangstück | |
| EP0436506A1 (de) | Vorrichtung zum Richten von Stapeln | |
| DE4315314A1 (de) | Vorrichtung zum Ändern der Stellung eines Deckels | |
| DE2002453B2 (de) | Greifer zum setzen von ziegelformlingen | |
| DE2236188B2 (de) | Fördervorrichtung | |
| DE3123073C1 (de) | Vorrichtung fuer das Giessen von Hohlgeschirr | |
| DE112004002697B4 (de) | Anlage zum Formen und Stapeln von Kalksandsteinrohlingen | |
| DE10394248T5 (de) | Anlage zum Formen und Stapeln von Kalksandsteinrohlingen | |
| DE69712439T2 (de) | Halter für keramische Produkte | |
| EP0187294A2 (de) | Pflasterstein | |
| EP0437858B1 (de) | Vorrichtung zum Herstellen von Oberflächenmuster aufweisenden Rohlingen für Klinkersteine, Ziegel und dgl. | |
| DE2614009A1 (de) | Umsetzvorrichtung zum ergreifen von stueckguetern | |
| DE3416019C2 (de) | Vorrichtung zum Transportieren von horizontal geteilten, kastenlosen Sandgießformen für Gießereizwecke | |
| EP1062169B1 (de) | Vorrichtung zur fahrzeugbeförderung mit mindestens zwei umlaufenden förderbändern | |
| EP0286778A2 (de) | Transport- und Behandlungsvorrichtung für mit giessfähiger, erstarrender Masse, wie Schokolade, füllbare Formen | |
| DE102015113740A1 (de) | Einrichtung und System zum Greifen und Handhaben von Objekten | |
| DE19720185A1 (de) | Wendeeinrichtung für Formkästen | |
| EP0224477B1 (de) | Vorrichtung zum transportieren von horizontal geteilten, kastenlosen sandgiessformen für giessereizwecke | |
| EP0736468B1 (de) | Vorrichtung zum Umsetzen von verformbaren, plattenförmigen Gegenständen, insbesondere Ziegelformlingen | |
| DE3507656C2 (de) | ||
| EP4088583B1 (de) | Produktträger und transportvorrichtung | |
| EP0110153B1 (de) | Brennschneidmaschine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): AT CH FR GB IT LI |
|
| 17P | Request for examination filed |
Effective date: 19821111 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): AT CH FR GB IT LI |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): AT CH FR GB IT LI |
|
| REF | Corresponds to: |
Ref document number: 10718 Country of ref document: AT Date of ref document: 19841215 Kind code of ref document: T |
|
| ET | Fr: translation filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Effective date: 19850608 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19850630 Ref country code: CH Effective date: 19850630 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19860228 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19881121 |