WO2015005503A2 - パッケージ及び製造方法 - Google Patents
パッケージ及び製造方法 Download PDFInfo
- Publication number
- WO2015005503A2 WO2015005503A2 PCT/JP2014/076182 JP2014076182W WO2015005503A2 WO 2015005503 A2 WO2015005503 A2 WO 2015005503A2 JP 2014076182 W JP2014076182 W JP 2014076182W WO 2015005503 A2 WO2015005503 A2 WO 2015005503A2
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- package
- absorbent articles
- packaging material
- skirt portion
- product
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D77/00—Packages formed by enclosing articles or materials in preformed containers, e.g. boxes, cartons, sacks or bags
- B65D77/04—Articles or materials enclosed in two or more containers disposed one within another
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/551—Packaging before or after use
- A61F13/55105—Packaging before or after use packaging of diapers
- A61F13/55115—Packaging before or after use packaging of diapers characterized by the features before use, e.g. how are the diapers folded or arranged in a package
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/551—Packaging before or after use
- A61F13/5513—Packaging before or after use packaging of feminine sanitary napkins
- A61F13/55135—Packaging before or after use packaging of feminine sanitary napkins before use
- A61F13/55145—Packaging before or after use packaging of feminine sanitary napkins before use multiple packaged items
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D75/00—Packages comprising articles or materials partially or wholly enclosed in strips, sheets, blanks, tubes or webs of flexible sheet material, e.g. in folded wrappers
- B65D75/04—Articles or materials wholly enclosed in single sheets or wrapper blanks
- B65D75/06—Articles or materials wholly enclosed in single sheets or wrapper blanks in sheets or blanks initially folded to form tubes
- B65D75/12—Articles or materials wholly enclosed in single sheets or wrapper blanks in sheets or blanks initially folded to form tubes with the ends of the tube closed by flattening and heat-sealing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2203/00—Decoration means, markings, information elements, contents indicators
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2577/00—Packages formed by enclosing articles or materials in preformed containers, e.g. boxes, cartons, sacks, bags
- B65D2577/04—Articles or materials enclosed in two or more containers disposed one within another
- B65D2577/041—Details of two or more containers disposed one within another
- B65D2577/042—Comprising several inner containers
- B65D2577/043—Comprising several inner containers arranged side by side
Definitions
- the present invention relates to a package and a manufacturing method.
- an object of the present invention is to provide a package that is conspicuous and difficult to fall down when displayed in a store, and a method for manufacturing the package.
- a first feature of the present invention is a package for packaging a plurality of absorbent articles in a folded state, formed of a film-shaped packaging material, and configured to enclose the plurality of absorbent articles.
- the absorbent article is provided with a bag portion that is enclosed in a folded state in the bag portion, and has a product longitudinal direction, a product width direction, and a product thickness direction that are orthogonal to each other.
- the bag portion has an up-down direction, a left-right direction, and a thickness direction orthogonal to each other, and the bag portion has a bottom surface formed at at least one end in the up-down direction, and the left-right direction.
- a fixing region where the packaging materials are fixed to each other is formed along the left-right direction, and at least one of the side surfaces,
- the packaging material A skirt portion that is fixed to the left and right direction is formed in an annular shape along an outer edge portion of the side surface, and the product thickness direction of each of the absorbent articles is within the bag portion.
- the gist is that the plurality of absorbent articles are accommodated in a state in which the product longitudinal direction or the product width direction of each of the absorbent articles is aligned with the left-right direction and the thickness direction is matched.
- the second feature of the present invention is a method of manufacturing a package for packaging a plurality of absorbent articles in a folded state, in which a continuous film-like packaging material conveyed in the conveying direction is wound into a cylindrical shape. Using a planographic plate or a roll, sandwiching both ends of the continuous body wound in the cylindrical shape in a direction orthogonal to the transport direction, and then sandwiching the continuous bodies along the transport direction And having a step of fixing.
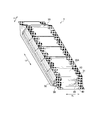
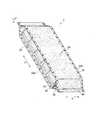
- FIG. 1 It is a perspective view of the package which concerns on the 1st Embodiment of this invention. It is the figure seen from the A side (side surface side) in FIG. It is a perspective view of the small package accommodated in the package which concerns on the 1st Embodiment of this invention. It is the top view and X-X 'cross section figure of the absorbent article accommodated in the small package accommodated in the package which concerns on the 1st Embodiment of this invention. It is a figure which shows an example of the accommodation state of the absorbent article in the small package accommodated in the package which concerns on the 1st Embodiment of this invention. It is a perspective view of the package which concerns on the example of a change of this invention.
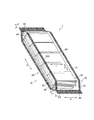
- FIG. 1 is a perspective view of a package 1 according to the present embodiment
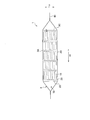
- FIG. 2 is a view as viewed from the A side (side surface side) in FIG. 1
- FIG. 3 is a diagram according to the first embodiment of the present invention.
- It is a perspective view of the small package 20 accommodated in the package 1 which concerns
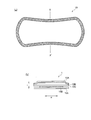
- Fig.4 (a) is accommodated in the small package 20 accommodated in the package 1 which concerns on the 1st Embodiment of this invention
- Fig. 4 (b) is a cross-sectional view taken along the line XX 'in Fig. 4 (a)
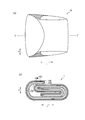
- Fig. 5 (a) shows the first embodiment of the present invention.
- FIG.5 (b) is YY 'sectional drawing in Fig.5 (a).
- the package 1 is configured to wrap a plurality of absorbent articles 10 in a folded state, and is formed by a film-like packaging material 3.
- a bag portion 25 configured to enclose a plurality of absorbent articles 10 is provided.
- each of the absorbent article 10 enclosed in the state folded in the bag part 25 is the product longitudinal direction L, the product width direction W, and the product thickness direction T orthogonal to each other. have.
- the length in the product longitudinal direction L is longer than the length in the product width direction W. It is comprised so that it may become.
- an arbitrary article such as a panty liner (origami sheet), a sanitary napkin or an incontinence pad is assumed.
- the bag part 25 has the up-down direction UD, the left-right direction RL, and the thickness direction TT which are orthogonal to each other.
- the length of the bag portion 25 in the vertical direction UP is longer than the length of the bag portion 25 in the left-right direction RL of the bag portion 25, that is, the bag portion 25 is It has a substantially rectangular parallelepiped shape.
- the bag portion 25 includes a front surface (or back surface) 2A and a back surface (or front surface) 2B formed at both end portions in the thickness direction TT, and at least the vertical direction UD. It has a bottom surface 2C / 2D formed at one end and side surfaces 2E / 2F formed at both ends in the left-right direction RL.
- the package 1 which concerns on this embodiment, it may be comprised so that a front surface and a back surface may be distinguished, and you may be comprised so that a front surface and a back surface may not be distinguished.
- the product thickness direction T of each absorbent article 10 matches the thickness direction TT and the product longitudinal direction L of each absorbent article 10 is within the bag portion 25.
- a plurality of absorbent articles 10 may be accommodated in a state where is aligned in the left-right direction.
- the product thickness direction T of each absorbent article 10 is aligned with the thickness direction TT, and the product width direction W of each absorbent article 10 is aligned with the left-right direction.
- the absorbent article 10 may be accommodated in a folded state.
- a fixing region 40 in which the packaging materials 3 are fixed to each other is formed along the left-right direction RL.
- the skirt part 30 to which the packaging materials 3 are adhering and which extends in the left-right direction RL is attached to the outer edge part of the side surface 2E / 2F in at least one of the side surfaces 2E / 2F. It is formed in an annular shape along.
- the packaging materials 3 are fixed to each other by a heat sheet or the like.
- the width (length in the left-right direction RL) fixed in the skirt portion 30 is preferably 1 mm or more. It is not necessary to adhere to the entire skirt portion 30.
- the sealing process may be performed linearly in the skirt portion 30.
- the rigidity of the packaging material 3 is small, it may be fixed over the entire surface of the skirt portion 30.
- the heat seal pattern may be any pattern such as a lattice shape, a solid push, or a linear shape.
- the height (that is, the length in the left-right direction RL) L1 of the skirt portion 30 is preferably 5 mm to 10 mm.
- the skirt portion 30 When the height of the skirt portion 30 is longer than 10 mm, the skirt portion 30 cannot withstand the load and buckles. On the other hand, when the height of the skirt portion 30 is shorter than 5 mm, the surface of the side surface 2E / 2F is rounded and thus cannot stand on its own.
- a gusset folding portion that is folded inward in the left-right direction RL of the bag portion 25 at the side edge portion in the left-right direction RL and both end portions in the up-down direction UD of the bag portion 25. 50 may be formed.
- a pillow-type bag shape may be used at the side edge portion of the bag portion 25 in the left-right direction RL.
- the package 1 according to the present embodiment may be configured to accommodate a plurality of small packages 20 in the bag portion 25.
- the five small packages 20 are accommodated in the bag part 25 of the package 1 which concerns on this embodiment.
- each of the small packages 20 is configured to accommodate a predetermined number of absorbent articles among the plurality of absorbent articles 10 in a product thickness direction T. ing.
- each of the small packages 20 is configured to accommodate six absorbent articles in the product thickness direction T in an overlapping manner.
- FIG. 3 is a perspective view of the small package 20.
- the small package 20 may have a bag portion 20 ⁇ / b> A having the same form as the bag portion 25 of the package 10.
- the packaging material 3 described above is made of a material that can be fixed by heat sealing before and after the flow direction in the manufacturing process.
- a film such as LDPE or HDPE (or a mixed film of LDPE and HDPE), a multilayer film such as PE / PET, PE / PP, or PE / M / PP, or a length of spunbond / SMS
- a fiber non-woven fabric, a PE film and a long-fiber non-woven fabric combined with a laminate, or the like may be used.
- bag portion 25 may be formed by overlapping two or more packaging materials 3 or may be formed in a form in which one packaging material 3 is wound.
- the bulk softness value of the packaging material 3 is preferably 0.5N to 100N, and more preferably 0.8N to 60N.
- the thickness of the packaging material 3 is preferably 10 ⁇ m to 500 ⁇ m.
- the package 1 when the value of the bulk softness of the packaging material 3 is too small (that is, when it is less than 0.5 N), or when the thickness of the packaging material 3 is too thin (that is, when it is less than 10 ⁇ m), It is difficult for the package 1 to stand on its own in the fixing region 40.
- the value of the bulk softness of the packaging material 3 is too large (that is, when it is larger than 100N), or when the thickness of the packaging material 3 is too thick (that is, when it is larger than 500 ⁇ m), it is added from the outside. Since heat is not easily transmitted to the inside, it is difficult to fix the film-like packaging materials 3 together.
- the measurement target material (packaging material 3) is cut into a size of 15 mm (left-right direction) ⁇ 100 mm (vertical direction), and the cut measurement target material is cylindrically shaped so that the height is 15 mm.
- the test sample is generated by rounding (one turn) and fixing the upper and lower two places with a stapler or the like on the part that is overlapped when rounded (the width of the part is 10 mm).
- the maximum load when the test sample is compressed is measured from the height direction described above, and the measurement result is set as the value of bulk softness.
- Compression tester Autograph 1 (compression simple mode) Method: Bulk softness Compression speed: 10mm / min
- the absorbent article 10 includes a top sheet 10A, an absorbent sheet 10B that is an airlaid sheet containing pulp and fibers, a back sheet 10C, and a release paper 10E.
- the release paper 10E is joined to the back sheet by the misalignment adhesive 10D.
- the plurality of absorbent articles 10 may be folded in three (see FIG. 5 (a) and FIG. 5 (b)), five or the like.
- the side surface 2E / 2F can be made self-supporting, and therefore, when displaying at a storefront, the package 1 can be made more self-supporting than when the bottom surface 2C / 2D is made self-supporting.
- the front is easily seen by consumers.
- the skirt portion 30 is formed by folding and bonding the film-shaped packaging material 3, so that the rigidity of the skirt portion 30 is higher than other portions, The independence of the package 1 is improved.
- the skirt portion 30 can stand on its own.
- a material 31 different from the packaging material 3 may be overlapped and bonded on the outer peripheral surface of the skirt portion 30.
- the material 31 different from the film-like packaging material 3 is adhered and overlapped, so that the width of the design attached to the package 1 is increased. Can be spread.
- a predetermined shape of a punching process may be performed at a predetermined portion 32 of the skirt portion 30.
- star-shaped punching is performed at a predetermined portion 32 on the outer peripheral surface between the outer edge portion 32 and the root portion 31 of the skirt portion 30.
- the predetermined portion 32 may be an arbitrary portion in the skirt portion 30.
- the shape of the punching process may be an arbitrary shape.
- the entire packaging material 3 on the front surface 2A of the bag portion 25 is fixed by heat sealing or the like.
- the predetermined portion 32 of the skirt portion 30 may be subjected to a predetermined shape cutting process or a predetermined shape embossing process.
- the predetermined portion 32 may be an arbitrary portion in the skirt portion 30. Furthermore, the shape of cut processing or embossing may be any shape. According to these structures, the package 1 excellent in design can be provided.
- a predetermined shape of sealing processing may be performed at a predetermined portion 33 of the skirt portion 30.
- a heart-shaped sealing process is applied to a predetermined portion 33 on the outer peripheral surface between the outer edge portion 32 and the root portion 31 of the skirt portion 30.
- the predetermined part 33 may be an arbitrary part in the skirt portion 30.
- the shape of the sealing process may be an arbitrary shape.
- the skirt portion 30 can be strengthened and the self-supporting property of the package 1 can be improved.
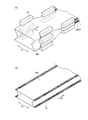
- the continuous body 300 of the film-form packaging material 3 currently conveyed by MD direction is wound in a cylinder shape.
- the packaging material is aligned along the conveyance direction MD.
- 3 continuums 300 are fixed to each other.
- the roll 60 is installed so as to sandwich the both end portions 300A forming the skirt portion 30.
- the fixing region 40 is formed, and the continuous body 300 of the packaging material 3 is cut into a predetermined length.
- the continuous body 300 of the film-form packaging material 3 currently conveyed by MD direction is wound in a cylinder shape.
- the fixing region 40 is formed, and the continuous body 300 of the packaging material 3 is cut into a predetermined length.
- the equipment structure can be simplified as compared with the manufacturing method 2 of the package 1 according to the present embodiment using the roll 60.
- the manufacturing method 2 of the package 1 according to the present embodiment it is possible to manufacture the package 1 having a lower skirt portion 30 than the manufacturing method 2 of the package 1 according to the present embodiment using the roll 60. it can.
- the present invention it is possible to provide a package that is easy to stand out and is not easily collapsed when displayed in a store, and a method for manufacturing the package.
Landscapes
- Health & Medical Sciences (AREA)
- Engineering & Computer Science (AREA)
- Epidemiology (AREA)
- Animal Behavior & Ethology (AREA)
- Public Health (AREA)
- Heart & Thoracic Surgery (AREA)
- Vascular Medicine (AREA)
- Life Sciences & Earth Sciences (AREA)
- Mechanical Engineering (AREA)
- General Health & Medical Sciences (AREA)
- Biomedical Technology (AREA)
- Veterinary Medicine (AREA)
- Packaging Of Annular Or Rod-Shaped Articles, Wearing Apparel, Cassettes, Or The Like (AREA)
- Packages (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Bag Frames (AREA)
- Absorbent Articles And Supports Therefor (AREA)
Abstract
本発明に係るパッケージ1では、底面2C/2Dにおいて、包装材3同士が固着されている固着領域40が、左右方向RLに沿って形成されており、側面2E/2Fの少なくとも一方において、包装材3同士が固着されており袋部25の左右方向RLに延出するスカート部30が、側面2E/2Fの外縁部に沿って環状に形成されており、袋部25内において、吸収性物品10の各々の製品厚み方向Tが袋部25の厚み方向Tに合っており且つ吸収性物品10の各々の製品長手方向L又は製品幅方向Wが左右方向RLに合っている状態で、複数の吸収性物品10が収容されている。
Description
本発明は、パッケージ及び製造方法に関する。
従来、パッケージを自立させるために、底面の外縁部から底面に略直交する方向に延出するスカート部が設けられている技術が知られている(特許文献1及び2参照)。
しかしながら、上述のパッケージでは、パンティーライナー等のような小さい吸収性物品を収容する場合には、正面の面積が小さいため、店舗内に陳列されている際に目立ちにくくなり、また、スカート部が底面に設けられているため、倒れやすいという問題点があった。
そこで、本発明は、このような状況に鑑みてなされたものであり、店舗内に陳列されている際に目立ちやすく且つ倒れにくいパッケージ及びパッケージの製造方法を提供することを目的とする。
本発明の第1の特徴は、折り畳まれた状態の複数の吸収性物品を包装するパッケージであって、フィルム状の包装材によって形成されており、前記複数の吸収性物品を封入するように構成されている袋部を具備しており、前記袋部内に折り畳まれた状態で封入されている前記吸収性物品は、互いに直交する製品長手方向と製品幅方向と製品厚み方向とを有しており、前記袋部は、互いに直交する上下方向と左右方向と厚み方向とを有しており、前記袋部は、前記上下方向の少なくとも一方の端部に形成されている底面と、前記左右方向の両端部に形成されている側面とを有しており、前記底面において、前記包装材同士が固着されている固着領域が、前記左右方向に沿って形成されており、前記側面の少なくとも一方において、前記包装材同士が固着されており前記左右方向に延出するスカート部が、前記側面の外縁部に沿って環状に形成されており、前記袋部内において、前記吸収性物品の各々の前記製品厚み方向が前記厚み方向に合っており且つ前記吸収性物品の各々の前記製品長手方向又は前記製品幅方向が前記左右方向に合っている状態で、前記複数の吸収性物品が収容されていることを要旨とする。
本発明の第2の特徴は、折り畳まれた状態の複数の吸収性物品を包装するパッケージの製造方法であって、搬送方向に搬送されているフィルム状の包装材の連続体を筒状に巻回する工程と、平版又はロールを用いて、前記筒状に巻回された前記連続体の前記搬送方向に直交する方向の両端部を挟み込んだ後、前記搬送方向に沿って前記連続体同士を固着する工程とを有することを要旨とする。
(第1の実施形態に係るパッケージ)
図1乃至図5を参照して、本発明の第1の実施形態に係るパッケージ1について説明する。
図1乃至図5を参照して、本発明の第1の実施形態に係るパッケージ1について説明する。
なお、以下の図面の記載において、同一又は類似の部分には、同一又は類似の符号を付している。ただし、図面は模式的なものであり、各寸法の比率等は現実のものとは異なることに留意すべきである。
したがって、具体的な寸法等は、以下の説明を参酌して判断すべきである。また、図面相互間においても互いの寸法の関係や比率が異なる部分が含まれ得る。
図1は、本実施形態に係るパッケージ1の斜視図であり、図2は、図1におけるA側(側面側)から見た図であり、図3は、本発明の第1の実施形態に係るパッケージ1内に収容されている小パッケージ20の斜視図であり、図4(a)は、本発明の第1の実施形態に係るパッケージ1内に収容されている小パッケージ20内に収容されている吸収性物品10の平面図であり、図4(b)は、図4(a)におけるX-X’断面図であり、図5(a)は、本発明の第1の実施形態に係るパッケージ1内に収容されている小パッケージ20内における吸収性物品10の収容状態を示す図であり、図5(b)は、図5(a)におけるY-Y’断面図である。
図1及び図2に示すように、本実施形態に係るパッケージ1は、折り畳まれた状態の複数の吸収性物品10を包装するように構成されており、フィルム状の包装材3によって形成されており複数の吸収性物品10を封入するように構成されている袋部25を具備している。
図1及び図2に示すように、袋部25内で折り畳まれた状態で封入されている吸収性物品10の各々は、互いに直交する製品長手方向Lと製品幅方向Wと製品厚み方向Tとを有している。
また、図1に示すように、かかる包装袋2内で折り畳まれた状態で収容されている吸収性物品10の各々において、製品長手方向Lの長さは、製品幅方向Wの長さよりも長くなるように構成されている。
ここで、本実施形態に係るパッケージ1に収容される吸収性物品10としては、パンティーライナー(おりものシート)や生理用ナプキンや失禁パッド等の任意の物品が想定される。
ここで、図1に示すように、袋部25は、互いに直交する上下方向UDと左右方向RLと厚み方向TTとを有している。
なお、本実施形態に係るパッケージ1では、袋部25の上下方向UPの長さは、袋部25の左右方向RLの袋部25の長さよりも長くなっている、すなわち、袋部25は、略直方体の形状を有している。
また、図1及び図2に示すように、袋部25は、厚み方向TTの両端部に形成されている正面(或いは、裏面)2A及び裏面(或いは、正面)2Bと、上下方向UDの少なくとも一方の端部に形成されている底面2C/2Dと、左右方向RLの両端部に形成されている側面2E/2Fとを有している。
なお、本実施形態に係るパッケージ1では、正面及び裏面が区別されるように構成されていてもよいし、正面及び裏面が区別されないように構成されていてもよい。
ここで、図1及び図2に示すように、袋部25内において、吸収性物品10の各々の製品厚み方向Tが厚み方向TTに合っており且つ吸収性物品10の各々の製品長手方向Lが左右方向に合っている状態で、複数の吸収性物品10が収容されていてもよい。
或いは、袋部25内において、吸収性物品10の各々の製品厚み方向Tが厚み方向TTに合っており且つ吸収性物品10の各々の製品幅方向Wが左右方向に合っている状態で、複数の吸収性物品10が折り畳まれた状態で収容されていてもよい。
図1及び図2に示すように、底面2C/2Dにおいて、包装材3同士が固着されている固着領域40が、左右方向RLに沿って形成されている。
また、図1及び図2に示すように、側面2E/2Fの少なくとも一方において、包装材3同士が固着されており左右方向RLに延出するスカート部30が、側面2E/2Fの外縁部に沿って環状に形成されている。
ここで、図1に示すように、スカート部30の根元部分30Aにおいて、ヒートシート等によって包装材3同士が固着されている。
例えば、スカート部30において固着されている幅(左右方向RLの長さ)は、1mm以上であることが好ましい。なお、スカート部30の全面に渡って固着する必要はない。例えば、スカート部30において線状にシール加工を施してもよい。
ただし、包装材3の剛性が小さい場合には、スカート部30の全面に渡って固着してもよい。
また、かかるヒートシールのパターンは、格子状、べた押し、線状等の任意のパターンであってもよい。
さらに、例えば、かかるスカート部30の高さ(すなわち、左右方向RLにおける長さ)L1は、5mm~10mmであることが好ましい。
かかるスカート部30の高さが、10mmよりも長くなると、スカート部30が、荷重に耐えられなくなり座屈してしまう。一方、かかるスカート部30の高さが、5mmよりも短くなると、側面2E/2Fの表面が丸みを帯びているため、自立することができなくなる。
さらに、図1及び図2に示すように、かかる袋部25の左右方向RLの側縁部かつ上下方向UDの両端部において、袋部25の左右方向RLの内側に向けて折り込んだガゼット折り込み部50が形成されていてもよい。
或いは、かかる袋部25の左右方向RLの側縁部において、ピロ方式の袋形態が用いられていてもよい。
また、図1及び図2に示すように、本実施形態に係るパッケージ1では、袋部25内に、複数の小パッケージ20を収容するように構成されていてもよい。図1及び図2の例では、本実施形態に係るパッケージ1の袋部25内に、5個の小パッケージ20が収容されている。
ここで、図1乃至図3に示すように、かかる小パッケージ20の各々は、複数の吸収性物品10のうちの所定数の吸収性物品を製品厚み方向Tに重ねて収容するように構成されている。
例えば、本実施形態に係るパッケージ1では、かかる小パッケージ20の各々は、6個の吸収性物品を製品厚み方向Tに重ねて収容するように構成されている。
図3に、かかる小パッケージ20の斜視図を示す。例えば、図3に示すように、かかる小パッケージ20は、パッケージ10の袋部25と同様の形態の袋部20Aを有していてもよい。
ここで、上述の包装材3は、製造工程における流れ方向の前後をヒートシールで固定可能な素材が用いられる。
例えば、かかる包装材3として、LDPEやHDPE等のフィルム(或いは、LDPE及びHDPEの混合フィルム)や、PE/PETやPE/PPやPE/M/PPといった多層フィルムや、スパンボンド/SMSの長繊維不織布や、PEフィルム及び長繊維不織布をラミネートにより複合したもの等が用いられてもよい。
また、上述の袋部25は、2枚以上の複数の包装材3を重ね合わせることによって形成されていてもよいし、1枚の包装材3を巻き込むような形で形成されていてもよい。
なお、包装材3のバルクソフトネスの値は、0.5N~100Nであることが好ましく、0.8N~60Nであることがより好ましい。また、包装材3の厚みは、10μm~500μmであることが好ましい。
なお、包装材3のバルクソフトネスの値が、小さすぎる場合(すなわち、0.5N未満である場合)、或いは、包装材3の厚みが、薄すぎる場合(すなわち、10μm未満である場合)、固着領域40でパッケージ1が自立しにくい。
一方、包装材3のバルクソフトネスの値が、大きすぎる場合(すなわち、100Nより大きい場合)、或いは、包装材3の厚みが、厚すぎる場合(すなわち、500μmより大きい場合)、外から加えた熱が内部に伝わりにくいので、フィルム状の包装材3同士を固着しにくい。
ここで、包装材3のバルクソフトネスの値を測定する方法の一例について説明する。
第1に、測定対象資材(包装材3)を、15mm(左右方向)×100mm(上下方向)の大きさにカットし、高さが15mmとなるように、カットした測定対象資材を円筒状に丸め(1回巻き)、丸めた際に重ね合わせた部分に(かかる部分の幅は10mmとする)上下2箇所をホッチキス等で固定することによって試験サンプルを生成する。
第2に、以下の条件で、上述の高さ方向から、かかる試験サンプルを圧縮した際の最大荷重を測定して、かかる測定結果をバルクソフトネスの値とする。
圧縮試験機:オートグラフ1(圧縮シンプルモード)
メソッド:バルクソフトネス
圧縮速度:10mm/分
メソッド:バルクソフトネス
圧縮速度:10mm/分
図4(a)、図4(b)、図5(a)及び図5(b)に、袋部25内に折り畳まれた状態で収容されている吸収性物品10(パンティーライナー)の一例を示す。
図4(b)に示すように、かかる吸収性物品10は、トップシート10Aと、パルプ及び繊維を含むエアレイドシートである吸収シート10Bと、バックシート10Cと、離型紙10Eとによって構成されている。ここで、離型紙10Eは、ズレ止め接着剤10Dによってバックシートに接合されている。
なお、かかる複数の吸収性物品10は、3つ折り(図5(a)及び図5(b)参照)や5つ折り等によって折り畳まれていてもよい。
本実施形態に係るパッケージ1によれば、側面2E/2Fを下にして自立させることができるので、店頭に陳列する際に、底面2C/2Dを下にして自立させる場合よりも、パッケージ1の正面が消費者から視認されやすくなる。
また、本実施形態に係るパッケージ1によれば、フィルム状の包装材3を折り返して接着することによってスカート部30を形成しているため、他の部位よりもスカート部30の剛性が高くなり、パッケージ1の自立性が向上する。
また、本実施形態に係るパッケージ1によれば、側面2E/2Fの表面が丸みを帯びている場合であっても、スカート部30によって自立することが可能となる。
(変更例)
以下、図6乃至図8を参照して、上述の第1の実施形態に係るパッケージ1の変更例について、上述の第1の実施形態に係るパッケージ1との相違点に着目して説明する。
以下、図6乃至図8を参照して、上述の第1の実施形態に係るパッケージ1の変更例について、上述の第1の実施形態に係るパッケージ1との相違点に着目して説明する。
図6に示すように、本発明の変更例に係るパッケージ1では、スカート部30の外周面において、包装材3とは異なる資材31が重なって接着されていてもよい。
かかる構成によれば、スカート部30の根元部分30Aをヒートシール等で固着する際に、フィルム状の包装材3とは異なる資材31を重ねて接着することで、パッケージ1に付するデザインの幅を広げることができる。
また、図7に示すように、本発明の変更例に係るパッケージ1では、スカート部30の所定部位32において、所定形状の打ち抜き加工が施されていてもよい。
図7の例では、スカート部30の外縁部32と根元部分31との間の外周面の所定部位32において星型の打ち抜き加工が施されている。なお、かかる所定部位32は、スカート部30内の任意の部位であってもよい。さらに、打ち抜き加工の形状は、任意の形状であってもよい。
また、図7の例では、袋部25における正面2Aの全面の包装材3が、ヒートシール等によって固着されている。
或いは、本発明の変更例に係るパッケージ1では、スカート部30の所定部位32において、所定形状のカット加工又は所定形状のエンボス加工が施されていてもよい。
なお、かかる所定部位32は、スカート部30内の任意の部位であってもよい。さらに、カット加工又はエンボス加工の形状は、任意の形状であってもよい。これらの構成によれば、デザイン性に長けたパッケージ1を提供することができる。
また、図8に示すように、本発明の変更例に係るパッケージ1では、スカート部30の所定部位33において、所定形状のシール加工が施されていてもよい。
図8の例では、スカート部30の外縁部32と根元部分31との間の外周面の所定部位33においてハート型のシール加工が施されている。なお、かかる所定部位33は、スカート部30内の任意の部位であってもよい。さらに、シール加工の形状は、任意の形状であってもよい。
かかる構成によれば、スカート部30を構成する資材の剛性が低い場合であっても、袋部25における正面2Aの全面の包装材3をヒートシール等によって固着した上で、所定部位32において、部分的な固着を行うことで、スカート部30を強化することができ、パッケージ1の自立性を向上させることができる。
(本発明の第1の実施形態に係るパッケージ1の製造方法)
図9及び図10を参照して、本発明の第1の実施形態に係るパッケージ1の製造方法について説明する。
図9及び図10を参照して、本発明の第1の実施形態に係るパッケージ1の製造方法について説明する。
まず、図9を参照して、本実施形態に係るパッケージ1の製造方法1の特徴的な部分について説明する。
第1に、MD方向に搬送されているフィルム状の包装材3の連続体300を筒状に巻回する。
第2に、ロール60を用いて、筒状に巻回された包装材3の連続体300の搬送方向MDに直交する方向CDの両端部300Aを挟み込んだ後、搬送方向MDに沿って包装材3の連続体300同士を固着する。
ここで、上下方向からシール加工を施すために、スカート部30を形成する両端部300Aを挟み込むようにロール60を設置する。
第3に、かかる包装材3の連続体300において、上述の固定領域40を形成すると共に、かかる包装材3の連続体300を所定長にカットする。
本実施形態に係るパッケージ1の製造方法1によれば、フロー系の加工を行うことができるので、ロール60を用いて、連続的にシール加工を施すことができる。
次に、図10を参照して、本実施形態に係るパッケージ1の製造方法2の特徴的な部分について説明する。
第1に、MD方向に搬送されているフィルム状の包装材3の連続体300を筒状に巻回する。
第2に、平板70を用いて、筒状に巻回された包装材3の連続体300の搬送方向MDに直交する方向CDの両端部300Aを挟み込んだ後、搬送方向MDに沿って包装材3の連続体300同士を固着する。
第3に、かかる包装材3の連続体300において、上述の固定領域40を形成すると共に、かかる包装材3の連続体300を所定長にカットする。
本実施形態に係るパッケージ1の製造方法2によれば、ロール60を用いる本実施形態に係るパッケージ1の製造方法2よりも、設備構造を簡素化することができる。
また、本実施形態に係るパッケージ1の製造方法2によれば、ロール60を用いる本実施形態に係るパッケージ1の製造方法2よりも、スカート部30の高さが低いパッケージ1を製造することができる。
以上、上述の実施形態を用いて本発明について詳細に説明したが、当業者にとっては、本発明が本明細書中に説明した実施形態に限定されるものではないということは明らかである。本発明は、特許請求の範囲の記載により定まる本発明の趣旨及び範囲を逸脱することなく修正及び変更態様として実施することができる。従って、本明細書の記載は、例示説明を目的とするものであり、本発明に対して何ら制限的な意味を有するものではない。
なお、日本国特許出願第2013-206628号(2013年10月1日出願)の全内容が、参照により、本願明細書に組み込まれている。
本発明によれば、店舗内に陳列されている際に目立ちやすく且つ倒れにくいパッケージ及びパッケージの製造方法を提供することができる。
1…パッケージ
3…包装材
10…吸収性物品
20…小パッケージ
25…袋部
30…スカート部
40…固着領域
2A、2B…正面(又は、裏面)
2C、2D…底面
2E、2F…側面
3…包装材
10…吸収性物品
20…小パッケージ
25…袋部
30…スカート部
40…固着領域
2A、2B…正面(又は、裏面)
2C、2D…底面
2E、2F…側面
Claims (8)
- 折り畳まれた状態の複数の吸収性物品を包装するパッケージであって、
フィルム状の包装材によって形成されており、前記複数の吸収性物品を封入するように構成されている袋部を具備しており、
前記袋部内に折り畳まれた状態で封入されている前記吸収性物品は、互いに直交する製品長手方向と製品幅方向と製品厚み方向とを有しており、
前記袋部は、互いに直交する上下方向と左右方向と厚み方向とを有しており、
前記袋部は、前記上下方向の少なくとも一方の端部に形成されている底面と、前記左右方向の両端部に形成されている側面とを有しており、
前記底面において、前記包装材同士が固着されている固着領域が、前記左右方向に沿って形成されており、
前記側面の少なくとも一方において、前記包装材同士が固着されており前記左右方向に延出するスカート部が、前記側面の外縁部に沿って環状に形成されており、
前記袋部内において、前記吸収性物品の各々の前記製品厚み方向が前記厚み方向に合っており且つ前記吸収性物品の各々の前記製品長手方向又は前記製品幅方向が前記左右方向に合っている状態で、前記複数の吸収性物品が収容されていることを特徴とするパッケージ。 - 前記複数の吸収性物品のうちの所定数の吸収性物品を前記製品厚み方向に重ねて収容する複数の小パッケージを収容するように構成されていることを特徴とする請求項1に記載のパッケージ。
- 前記スカート部の外周面において、前記包装材とは異なる資材が重なって接着されていることを特徴とする請求項1又は2に記載のパッケージ。
- 前記スカート部の所定部位において、所定形状の打ち抜き加工が施されていることを特徴とする請求項1又は2に記載のパッケージ。
- 前記スカート部の所定部位において、所定形状のカット加工が施されていることを特徴とする請求項1又は2に記載のパッケージ。
- 前記スカート部の所定部位において、所定形状のエンボス加工が施されていることを特徴とする請求項1又は2に記載のパッケージ。
- 前記包装材のバルクソフトネスの値は、0.5N~100Nであることを特徴とする請求項1乃至6のいずれか一項に記載のパッケージ。
- 折り畳まれた状態の複数の吸収性物品を包装するパッケージの製造方法であって、
搬送方向に搬送されているフィルム状の包装材の連続体を筒状に巻回する工程と、
平版又はロールを用いて、前記筒状に巻回された前記連続体の前記搬送方向に直交する方向の両端部を挟み込んだ後、前記搬送方向に沿って前記連続体同士を固着する工程とを有することを特徴とする製造方法。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201480054465.3A CN105636881B (zh) | 2013-10-01 | 2014-09-30 | 包装体的制造方法 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2013206628A JP6219657B2 (ja) | 2013-10-01 | 2013-10-01 | パッケージ及び製造方法 |
| JP2013-206628 | 2013-10-01 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| WO2015005503A2 true WO2015005503A2 (ja) | 2015-01-15 |
| WO2015005503A3 WO2015005503A3 (ja) | 2015-03-12 |
Family
ID=52280689
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2014/076182 Ceased WO2015005503A2 (ja) | 2013-10-01 | 2014-09-30 | パッケージ及び製造方法 |
Country Status (3)
| Country | Link |
|---|---|
| JP (1) | JP6219657B2 (ja) |
| CN (1) | CN105636881B (ja) |
| WO (1) | WO2015005503A2 (ja) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113891843A (zh) * | 2019-09-25 | 2022-01-04 | 大王制纸株式会社 | 包装袋 |
| IT202100009416A1 (it) * | 2021-04-14 | 2022-10-14 | Premium Italia Srl | Dispositivo di confezionamento per prodotti monouso ad uso alimentare |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP6576972B2 (ja) * | 2017-03-31 | 2019-09-18 | 大王製紙株式会社 | フィルム包装ティシュー |
| JP2023178125A (ja) * | 2022-06-03 | 2023-12-14 | ユニ・チャーム株式会社 | 衛生物品の収容体、及び、衛生物品の収容体群 |
Family Cites Families (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5659506U (ja) * | 1979-10-13 | 1981-05-21 | ||
| JP3149158B2 (ja) * | 1995-03-28 | 2001-03-26 | 花王株式会社 | 吸収性物品の包装構造 |
| JPH1135079A (ja) * | 1997-07-15 | 1999-02-09 | Dainippon Printing Co Ltd | ウェットティッシュ用容器 |
| JP4749568B2 (ja) * | 2001-03-01 | 2011-08-17 | 出光ユニテック株式会社 | 易開封包装袋 |
| JP4118568B2 (ja) * | 2002-01-25 | 2008-07-16 | 株式会社彫刻プラスト | ヒダ付き縦ピロー包装体の製造方法 |
| AU2002367107B2 (en) * | 2001-12-25 | 2006-08-10 | Chokoku Plast Corporation | Self-standing packaging bag, packaging body, web roll, and manufacturing method therefor |
| JP4689193B2 (ja) * | 2004-05-28 | 2011-05-25 | ユニ・チャーム株式会社 | 包装体 |
| GB2421013B (en) * | 2004-12-10 | 2007-07-11 | Amcor Flexibles Europe As | Packaging with an openable top wall |
| US7225599B2 (en) * | 2005-04-05 | 2007-06-05 | Sealed Air Corporation | Apparatus and method for forming inflated articles |
| JP4875877B2 (ja) * | 2005-09-28 | 2012-02-15 | 株式会社東京自働機械製作所 | ヘム付き袋製袋装置 |
| WO2009016572A1 (en) * | 2007-08-02 | 2009-02-05 | The Iams Company | Burst resistant side gusseted bag |
| JP5224897B2 (ja) * | 2008-05-08 | 2013-07-03 | 株式会社フジシールインターナショナル | 自立袋 |
| EP2258628A1 (en) * | 2009-06-05 | 2010-12-08 | The Procter & Gamble Company | Plastic bag for stacked soft hygienic products |
| JP2010284928A (ja) * | 2009-06-12 | 2010-12-24 | Idemitsu Unitech Co Ltd | ジッパーテープ付包装袋の製造方法およびその製造装置 |
| JP5551405B2 (ja) * | 2009-10-15 | 2014-07-16 | 花王株式会社 | 包装体及び包装袋 |
| JP5568296B2 (ja) * | 2009-12-25 | 2014-08-06 | 株式会社川島製作所 | 縦型製袋充填包装機における製袋充填筒 |
| JP5961613B2 (ja) * | 2010-08-20 | 2016-08-02 | ザ・スカイライフ・カンパニー・インク | 物資供給パックと物資供給パックを製造する方法およびシステム |
| JP6132458B2 (ja) * | 2011-06-20 | 2017-05-24 | 凸版印刷株式会社 | 易カット性パウチ |
-
2013
- 2013-10-01 JP JP2013206628A patent/JP6219657B2/ja not_active Expired - Fee Related
-
2014
- 2014-09-30 WO PCT/JP2014/076182 patent/WO2015005503A2/ja not_active Ceased
- 2014-09-30 CN CN201480054465.3A patent/CN105636881B/zh active Active
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113891843A (zh) * | 2019-09-25 | 2022-01-04 | 大王制纸株式会社 | 包装袋 |
| CN113891843B (zh) * | 2019-09-25 | 2023-11-07 | 大王制纸株式会社 | 包装袋 |
| IT202100009416A1 (it) * | 2021-04-14 | 2022-10-14 | Premium Italia Srl | Dispositivo di confezionamento per prodotti monouso ad uso alimentare |
Also Published As
| Publication number | Publication date |
|---|---|
| JP6219657B2 (ja) | 2017-10-25 |
| CN105636881A (zh) | 2016-06-01 |
| JP2015071427A (ja) | 2015-04-16 |
| WO2015005503A3 (ja) | 2015-03-12 |
| CN105636881B (zh) | 2018-09-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109747957B (zh) | 包装件、可成形为所述包装件的包装件坯料以及边封袋 | |
| JP6144366B2 (ja) | 吸収性物品の包装体を把束する方法 | |
| US9520150B2 (en) | Flexible package and method of making same | |
| JP6219657B2 (ja) | パッケージ及び製造方法 | |
| JP6195289B2 (ja) | 包装袋 | |
| US8584855B2 (en) | Packaging pouch for absorbent article | |
| JP2013048786A (ja) | 吸収性物品の包装体 | |
| CN103356341A (zh) | 吸收性物品的包装体 | |
| CN106535851A (zh) | 用于卫生物品的包装单元及用于形成包装单元的方法 | |
| WO2011083854A1 (ja) | 吸収性物品の連続包装体 | |
| JP6068299B2 (ja) | パッケージ | |
| JP2016166030A (ja) | 袋体、包装体及び袋体の製造方法 | |
| CN105980260A (zh) | 用于皂条的包装件 | |
| JP6114018B2 (ja) | 連続包装体 | |
| CN104039287A (zh) | 用于制备吸收制品的方法 | |
| JP6138903B1 (ja) | 吸収性物品の製造方法 | |
| JP5600494B2 (ja) | 包装箱 | |
| US20250352411A1 (en) | Package of absorbent sanitary articles, method and machine for packaging absorbent sanitary articles | |
| JP2017132489A (ja) | 包装体および包装体用原反 | |
| JP6456072B2 (ja) | ドリップシート包装品及びその製造方法 | |
| JP2020070042A (ja) | ラベルロール梱包体 | |
| ITFI20090055A1 (it) | Procedimento per la realizzazione di sacchi in film di materia plastica destinati a confezioni con maniglia | |
| JP2011006139A (ja) | 情報伝達票付き包装体 | |
| JP2008297004A (ja) | ピロー包装用原反及びピロー包装体 | |
| KR20260000112A (ko) | 흡수용품을 포장하기 위한 파우치 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 14823440 Country of ref document: EP Kind code of ref document: A2 |
|
| NENP | Non-entry into the national phase in: |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: IDP00201602566 Country of ref document: ID |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 14823440 Country of ref document: EP Kind code of ref document: A2 |