EP4056337B1 - Verfahren zum konturstanzen eines ausgangsstapels aus blättrigem gut sowie stanzvorrichtung zur durchführung des verfahrens - Google Patents
Verfahren zum konturstanzen eines ausgangsstapels aus blättrigem gut sowie stanzvorrichtung zur durchführung des verfahrens Download PDFInfo
- Publication number
- EP4056337B1 EP4056337B1 EP21162102.4A EP21162102A EP4056337B1 EP 4056337 B1 EP4056337 B1 EP 4056337B1 EP 21162102 A EP21162102 A EP 21162102A EP 4056337 B1 EP4056337 B1 EP 4056337B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- punching
- contour
- stack
- blade
- punching blade
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F1/00—Perforating; Punching; Cutting-out; Stamping-out; Apparatus therefor
- B26F1/38—Cutting-out; Stamping-out
- B26F1/44—Cutters therefor; Dies therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D7/18—Means for removing cut-out material or waste
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F1/00—Perforating; Punching; Cutting-out; Stamping-out; Apparatus therefor
- B26F1/38—Cutting-out; Stamping-out
- B26F1/40—Cutting-out; Stamping-out using a press, e.g. of the ram type
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D2007/0012—Details, accessories or auxiliary or special operations not otherwise provided for
- B26D2007/0018—Trays, reservoirs for waste, chips or cut products
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D7/06—Arrangements for feeding or delivering work of other than sheet, web, or filamentary form
- B26D7/0675—Arrangements for feeding or delivering work of other than sheet, web, or filamentary form specially adapted for piles of sheets
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F1/00—Perforating; Punching; Cutting-out; Stamping-out; Apparatus therefor
- B26F1/38—Cutting-out; Stamping-out
- B26F1/40—Cutting-out; Stamping-out using a press, e.g. of the ram type
- B26F2001/407—Cutting-out; Stamping-out using a press, e.g. of the ram type stepwise sequential punching processes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F1/00—Perforating; Punching; Cutting-out; Stamping-out; Apparatus therefor
- B26F1/38—Cutting-out; Stamping-out
- B26F1/44—Cutters therefor; Dies therefor
- B26F2001/4481—Cutters therefor; Dies therefor having special lateral or edge outlines or special surface shapes, e.g. apertures
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F2210/00—Perforating, punching, cutting-out, stamping-out, severing by means other than cutting of specific products
- B26F2210/02—Perforating, punching, cutting-out, stamping-out, severing by means other than cutting of specific products of stacked sheets
Definitions
- the present invention relates to a method for contour punching an initial stack of sheet material, in particular for punching out labels from an initial stack of sheet material.
- the invention further relates to a punching device for carrying out the method.
- the method according to the invention and the device according to the invention are used in particular for punching an initial stack formed from a large number of sheets lying one above the other and provided with a label print.
- the initial stack of sheet material consists in particular of printed paper.
- the individual labels are made of plastic, in particular a plastic film.
- the initial stack to be punched is in particular a pre-cut stack of panels that has a cuboid shape.
- the method or the device serves to give the pre-cut stack of benefits its final contour.
- Labels are usually printed on large printed sheets that are stacked on top of each other to form several hundred to over 1,000 sheets. Such stacks of printed sheets are pre-cut lengthwise and crosswise, thereby forming a large number of pre-cut stacks of sheets then be isolated.
- a contour punching knife with a closed contour also known as a punching iron, is used. The punching is carried out in such a way that the stack to be punched is pressed against the contour punching knife, so that it is pushed into the contour punching knife, resulting in punching waste.
- the EP 1 584 432 B1 discloses such a method for contour punching an initial stack of sheet material and a punching device for carrying out the method.
- the DE 40 130 71 A1 discloses a device for contour punching with a contour punching knife, wherein the device has a punch that can be moved in the direction of the first contour punching knife for pressing an initial stack into the first contour punching knife and the device has a collecting device for collecting the punching waste.
- a further object of the invention is to create a device for carrying out the method according to the invention.
- the initial stack of leafy material, in particular the respective sheet, preferably has a cuboid shape.
- the output stack can in particular be a pre-cut output stack, the output stack being pre-cut in such a way that on the respective sheet there is only a single closed printed area per sheet of the pre-cut output stack, in particular a single label print per sheet of the pre-cut output stack .
- the label print forms the printed area. It is entirely conceivable that the printed area partially extends to the edge of the respective sheet.
- the label print preferably has larger dimensions than the final label.
- the pre-punched stack is pressed into the second contour punching knife by the initial stack acting on the pre-punched stack when the initial stack is pressed into the first contour punching knife. This means it is not necessary to handle the pre-punched stack separately.
- there are guide structures between the first contour punching knife and the second contour punching knife these guide structures serving to control the movement of the pre-punched stack when pressing the pre-punched stack in the direction of the second contour punching knife.
- the punching device is used to carry out the method according to the invention.
- the punching device has a first contour punching knife with a punching contour, a second contour punching knife with a punching contour and a punch that can be moved in the direction of the first contour punching knife for pressing an initial stack into the first contour punching knife.
- the dimensions of the punching contour of the first contour punching knife are larger than the dimensions of the punching contour of the second contour punching knife.
- the device has a first collecting device for collecting the first punching waste formed when the first contour punching knife passes through the initial stack.
- the second contour punching knife is arranged downstream of the first contour punching knife in the direction of travel of the punching stamp, so that the pre-punched stack is pressed into the second contour punching knife when the punching stamp is moved in the direction of the first contour punching knife.
- the device has a second collecting device for collecting the second punching waste formed when the second contour punching knife passes through the pre-punched stack.
- the first collecting device and the second collecting device are not identical, so that the first punching waste and the second punching waste are collected separately from each other.
- first and second collection devices are components of a common waste collection device, for example the collection devices are formed by different compartments of the waste collection device.
- a geometric shape of the punching contour of the first contour punching knife can be converted into a geometric shape of the punching contour of the second contour punching knife by scaling, with a scaling factor being less than 1.
- both the geometric shape of the punching contour of the first contour punching knife and the geometric shape of the punching contour of the second contour punching knife correspond, at least essentially, to the geometric shape of the outer contour of the printed area.
- contour punching knives are arranged nested one inside the other.
- both the first contour punching knife and the second contour punching knife are essentially hollow conical.
- the second contour punching knife can be arranged within the first contour punching knife.
- the punching device has at least one diverting element for diverting the first punching waste into the first collecting device and/or for diverting the second punching waste into the second collecting device.
- This diverting element can be, for example, a plate-shaped element, for example in the form of a partition. It is entirely conceivable and preferred for the diverting element to extend between the two contour punching knives in the direction of the collecting devices.
- the first collecting device and/or the second collecting device is a waste container, in particular a rollable waste container.
- the waste container is preferably a commercially available garbage can.
- the device has waste containers that can be handled separately from one another.
- first contour punching knife and/or the second contour punching knife is mounted in the punching device in a displaceable and/or pivotable manner, in particular if the contour punching knives are mounted in the punching device in a displaceable and/or pivotable manner relative to one another.
- the position of the first contour punching knife and/or the second contour punching knife can be changed in a particularly simple manner, in particular in order to achieve an optimal alignment of the respective contour punching knife to the initial stack or the pre-punched stack and/or the punch.
- first contour punching knife and/or the second contour punching knife are mounted in a common bearing structure, the bearing structure being pivotably and/or displaceably mounted in the punching device. This makes it possible to align the first contour punching knife and the second contour punching knife together, in particular to align them with respect to the initial stack. In this context, it is entirely conceivable that the position and orientation of the first contour punching knife relative to the second contour punching knife is unchangeable.
- first contour punching knife and/or the second contour punching knife is mounted in the bearing structure in a displaceable and/or pivotable manner.
- the punching contour of the first contour punching knife and/or the punching contour of the second contour punching knife are designed as a closed contour.
- the Fig. 1 and 2 show a punching device according to the invention, the punching device having a first contour punching knife 7 with a punching contour 8, a second contour punching knife 9 with a punching contour 10 and a punching punch 15 which can be moved in the travel direction X.
- the punch 15 can be moved by means of the drive 16.
- the punch 15 is used to press an initial stack 1 into the first contour punching knife 7.
- the initial stack 1 is formed from several sheets stacked one on top of the other and is pre-cut in such a way that it is cuboid and a single label print 20 is printed on the respective sheet.
- the respective sheet or the respective sheet 3 has a printed area 4, namely the label print 20, and an unprinted area 5 surrounding the printed area 4, the printed area 4 having an outer contour 6.
- the label print 20 has slightly larger dimensions than the final trimmed label 2.
- the label 2 is a label 2 for the neck area of a bottle.
- the punching contour 8 of the first contour punching knife 7 and the punching contour 10 of the second contour punching knife 9 can be approximately converted into one another by scaling, the punching contour 8 of the first contour punching knife 7 being slightly larger than the outer contour 6 of the printed area 4 and the punching contour 10 of the second contour punching knife 9 is slightly smaller than the outer contour 6 of the printed area 4.
- the punching contour 10 of the second contour punching knife 9 corresponds to an outer contour of the final label 2.
- the output stack 1 is moved in the direction of the first contour punching knife 7 by means of the punch 15 and pressed into the contour punching knife 7 in such a way that a pre-punched stack 11 is formed.
- the first punching waste 12 formed during this punching process is collected in a first collecting device 17, which is arranged below the first contour punching knife 7.
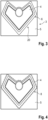
- the first contour punching knife 7 penetrates the output stack 1 exclusively in the unprinted area 5 of the output stack 1 or the respective sheet 3, as shown schematically in the Fig. 4 is shown. In this respect, the first punching waste 12 formed during this first punching process is free of printed areas.
- the punching device is designed in such a way that the pressing of the pre-punched stack 11 into the second contour punching knife 9 takes place in that the output stack 1 acts on the pre-punched stack 11 by means of the punching stamp 15 when the output stack 1 is pressed into the first contour punching knife 7 and this into the second Contour punching knife 9 presses.
- a stack of benefits 13 is formed from finally punched labels 2.
- the second contour punching knife 9 penetrates the pre-punched stack 11 exclusively in the printed area 4, so that the second punching waste 14 formed during this second punching process has printed areas 4 and unprinted areas 5.
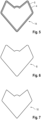
- this second punching waste 14 is for a single sheet 3 in the Fig. 5 shown.
- the Indian Fig. 5 Punching waste 14 shown is ring-shaped with an inner printed area 4 and an unprinted area 5 surrounding the printed area 4 radially on the outside.
- the punching device has a second collecting device 18 for collecting the second punching waste 14 formed during the second punching process.
- the punching device has two diverting elements 19, one of which is the diverting elements 19 extends from the first contour punching knife 7 in the direction of adjacent side walls of the collecting devices 17, 18 and the other diverting element 19 extends from the second contour punching knife 9 in the direction of a side wall of the second collecting device 18 opposite the adjacent side wall.
- This punching device thus ensures that only unprinted first punching waste 12 is collected in the first collecting device 17, which can be disposed of separately from the at least partially printed second punching waste 14, which is collected in the second collecting device 18.
- the cost of waste disposal can be reduced, since typically the cost of disposing of printed material is more expensive than disposing of unprinted material.
- the unprinted material can certainly be resold as a recyclable material. This means that money can be saved overall by separating printed and unprinted waste material.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Forests & Forestry (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
- Making Paper Articles (AREA)
- Sheets, Magazines, And Separation Thereof (AREA)
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP21162102.4A EP4056337B1 (de) | 2021-03-11 | 2021-03-11 | Verfahren zum konturstanzen eines ausgangsstapels aus blättrigem gut sowie stanzvorrichtung zur durchführung des verfahrens |
| ES21162102T ES2967366T3 (es) | 2021-03-11 | 2021-03-11 | Procedimiento para el troquelado de contorno de una pila inicial de material en hojas, así como dispositivo de troquelado para la realización del procedimiento |
| PL21162102.4T PL4056337T3 (pl) | 2021-03-11 | 2021-03-11 | Sposób wykrawania konturowego stosu wyjściowego materiału arkuszowego i urządzenie wykrawające do przeprowadzania sposobu |
| CN202210237756.2A CN115070868B (zh) | 2021-03-11 | 2022-03-11 | 对初始堆叠进行轮廓冲裁的方法和执行该方法的冲裁装置 |
| US17/692,245 US11992966B2 (en) | 2021-03-11 | 2022-03-11 | Method for contour punching an output stack and punching device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP21162102.4A EP4056337B1 (de) | 2021-03-11 | 2021-03-11 | Verfahren zum konturstanzen eines ausgangsstapels aus blättrigem gut sowie stanzvorrichtung zur durchführung des verfahrens |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP4056337A1 EP4056337A1 (de) | 2022-09-14 |
| EP4056337B1 true EP4056337B1 (de) | 2023-09-27 |
Family
ID=74871294
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP21162102.4A Active EP4056337B1 (de) | 2021-03-11 | 2021-03-11 | Verfahren zum konturstanzen eines ausgangsstapels aus blättrigem gut sowie stanzvorrichtung zur durchführung des verfahrens |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US11992966B2 (pl) |
| EP (1) | EP4056337B1 (pl) |
| CN (1) | CN115070868B (pl) |
| ES (1) | ES2967366T3 (pl) |
| PL (1) | PL4056337T3 (pl) |
Family Cites Families (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DK149424C (da) * | 1981-07-10 | 1986-11-17 | Bording Grafik As | Stanseapparat til udstansning af emner med kurvede eller buede kanter fra arkformet materiale, navnlig etiketter og lignende tryksagsemner |
| DE3628301A1 (de) * | 1986-08-21 | 1988-02-25 | Gerhard Busch | Pressbalken fuer schneidstanzen, mit variabler anpresslinie |
| DE4013071A1 (de) * | 1990-04-21 | 1991-06-13 | Gerhard Busch Gmbh Graphische | Vertkale stanzvorrichtung |
| CH689275A5 (de) * | 1994-10-20 | 1999-01-29 | Blumer Maschbau Ag | Vorrichtung und Verfahren zum Stanzen eines Stapels. |
| DE10023932A1 (de) * | 2000-05-17 | 2001-11-22 | Mohr Adolf Maschf | Vorrichtung zum Stanzen eines Stapels aus blättrigem Gut |
| DE502004010107D1 (de) * | 2004-03-08 | 2009-11-05 | Mohr Adolf Maschf | Stanze zum konturenstanzen eines vorgeschnittenen nutzenstapels |
| DE502004001339D1 (de) * | 2004-03-08 | 2006-10-12 | Mohr Adolf Maschf | Stanze zum Konturenstanzen eines vorgeschnittenen Nutzenstapels |
| EP1584432B1 (de) | 2004-03-08 | 2007-03-07 | Adolf Mohr Maschinenfabrik GmbH & Co. KG | Stanze zum Konturenstanzen eines vorgeschnittenen Nutzenstapels |
| WO2014110079A1 (en) * | 2013-01-08 | 2014-07-17 | Tek Industries, Inc. | Multi-die cut with common axis |
| CH709659A1 (de) * | 2014-05-15 | 2015-11-30 | Blumer Maschb Ag | Verfahren zum Zuschneiden von Etikettenausgangsstapel. |
| BE1022742B1 (nl) * | 2015-02-24 | 2016-08-26 | VERSTRAETE IN MOULD LABELS, naamloze vennootschap | Automatische stansmachine. |
| CH714638A2 (de) * | 2018-02-12 | 2019-08-15 | Blumer Maschb Ag | Stanzvorrichtung zur Herstellung von Formetiketten. |
| CN112571505B (zh) * | 2020-11-19 | 2024-03-08 | 西安雄峰印刷包装有限公司 | 一种标签生产系统 |
-
2021
- 2021-03-11 PL PL21162102.4T patent/PL4056337T3/pl unknown
- 2021-03-11 ES ES21162102T patent/ES2967366T3/es active Active
- 2021-03-11 EP EP21162102.4A patent/EP4056337B1/de active Active
-
2022
- 2022-03-11 US US17/692,245 patent/US11992966B2/en active Active
- 2022-03-11 CN CN202210237756.2A patent/CN115070868B/zh active Active
Also Published As
| Publication number | Publication date |
|---|---|
| PL4056337T3 (pl) | 2025-01-13 |
| EP4056337A1 (de) | 2022-09-14 |
| CN115070868A (zh) | 2022-09-20 |
| CN115070868B (zh) | 2026-03-03 |
| US11992966B2 (en) | 2024-05-28 |
| US20220288803A1 (en) | 2022-09-15 |
| ES2967366T3 (es) | 2024-04-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2805125C2 (de) | Verfahren zur Herstellung von Umschlägen mit mehreren Einlageblättern | |
| EP4069479B1 (de) | Vorrichtung und verfahren zur nutzentrennung | |
| EP1914049B1 (de) | Flachbett-Bogenstanzmaschine | |
| DE3243661C2 (de) | Trennvorrichtung | |
| EP1005984A1 (de) | Verfahren zur Herstellung gefalteter, gebundener Druckerzeugnisse sowie Druckerzeugnis | |
| EP3437815B1 (de) | Rotationsstanze zum ausstanzen eines materialstücks aus einem bedruckstoff | |
| EP4069480B1 (de) | Vorrichtung und verfahren zur nutzentrennung | |
| DE69303154T2 (de) | Heftklammern für Papier und Herstellungsverfahren | |
| EP4116007A1 (de) | Abfalltrennvorrichtung und verfahren zur auftrennung eines stanzgitters | |
| DE102009033575A1 (de) | Folienmesser mit Saugkammer | |
| AT392753B (de) | Nutzentrennung zur verwendung in verbindung mit einer vorrichtung zum stanzen von boegen aus papier, karton od.dgl. | |
| EP0068228A1 (de) | Gefalzter oder zum Falzen bestimmter Druckbogen | |
| EP3509806B1 (de) | Verfahren zur bearbeitung eines substrats mit einem stanzstempel | |
| EP1140517B1 (de) | Sammelheftmaschine und verfahren zum herstellen eines aufschlagregisters an mittels einer sammelheftmaschine zu heftenden druck- oder papierwerken | |
| DE102009034437A1 (de) | Vorrichtung und Verfahren zur Ausbildung einer Kontur in einem Kartenkörper für einen tragbaren Datenträger, insbesondere für eine Chipkarte | |
| EP4056337A1 (de) | Verfahren zum konturstanzen eines ausgangsstapels aus blättrigem gut sowie stanzvorrichtung zur durchführung des verfahrens | |
| DE102010024771A1 (de) | Schneide- und Stanzeinrichtung | |
| DE102009028003A1 (de) | Stanzwerkzeug zum Herstellen von Zuschnitten aus Karton, Pappe, Schaumstoff oder dergleichen | |
| DE4428185A1 (de) | Vorrichtung zum Herstellen von Aufreißperforationen | |
| DE10156664B4 (de) | Vorrichtung zum rotierenden Stanzen von Nutzen aus Einzelbögen | |
| DE2922088C2 (de) | Verfahren und Vorrichtung zur Herstellung von Blattstapeln, Blocks o.dgl. | |
| EP4303026B1 (de) | Verfahren und vorrichtung zur erstellung eines booklets | |
| DE3147968C2 (de) | Vorrichtung zur Herstellung kreisförmiger oder anders geformter Spitzenpapiere | |
| DE10047496C2 (de) | Verfahren zum Durchtrennen insbesondere Lochen einer Sandwichplatte und dafür geeignetes Stanzwerkzeug | |
| DE69216095T2 (de) | Blätter mit reiter oder merkzeichen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20230214 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B26F 1/38 20060101ALI20230321BHEP Ipc: B26D 7/18 20060101AFI20230321BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20230413 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230821 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502021001540 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20231228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20231227 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20231228 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240127 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2967366 Country of ref document: ES Kind code of ref document: T3 Effective date: 20240429 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240127 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240129 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20240304 Year of fee payment: 4 Ref country code: FR Payment date: 20240328 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502021001540 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20240429 Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20240401 Year of fee payment: 4 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20240628 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240311 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240311 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20240331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240331 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20240304 Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240311 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240311 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240331 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 502021001540 Country of ref document: DE Owner name: POLAR-MOHR BETEILIGUNGS GMBH, DE Free format text: FORMER OWNER: ADOLF MOHR MASCHINENFABRIK GMBH & CO. KG, 65719 HOFHEIM, DE Ref country code: DE Ref legal event code: R081 Ref document number: 502021001540 Country of ref document: DE Owner name: HEIDELBERGER DRUCKMASCHINEN AKTIENGESELLSCHAFT, DE Free format text: FORMER OWNER: ADOLF MOHR MASCHINENFABRIK GMBH & CO. KG, 65719 HOFHEIM, DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20240304 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20250401 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20210311 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20210311 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250311 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20250311 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: R14 Free format text: ST27 STATUS EVENT CODE: U-0-0-R10-R14 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20251127 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 1614954 Country of ref document: AT Kind code of ref document: T Owner name: POLAR-MOHR BETEILIGUNGS GMBH, DE Effective date: 20251027 Ref country code: DE Ref legal event code: R081 Ref document number: 502021001540 Country of ref document: DE Owner name: HEIDELBERGER DRUCKMASCHINEN AKTIENGESELLSCHAFT, DE Free format text: FORMER OWNER: POLAR-MOHR BETEILIGUNGS GMBH, 65719 HOFHEIM, DE Ref country code: DE Ref legal event code: R082 Ref document number: 502021001540 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250311 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250331 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250311 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: U11 Free format text: ST27 STATUS EVENT CODE: U-0-0-U10-U11 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260401 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20260331 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20260319 Year of fee payment: 6 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 1614954 Country of ref document: AT Kind code of ref document: T Owner name: HEIDELBERGER DRUCKMASCHINEN AG, DE Effective date: 20260216 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20260424 |