EP2591223B1 - Verfahren zur herstellung eines zylinders für einen zweitaktmotor sowie gusskern hierfür - Google Patents
Verfahren zur herstellung eines zylinders für einen zweitaktmotor sowie gusskern hierfür Download PDFInfo
- Publication number
- EP2591223B1 EP2591223B1 EP11808135.5A EP11808135A EP2591223B1 EP 2591223 B1 EP2591223 B1 EP 2591223B1 EP 11808135 A EP11808135 A EP 11808135A EP 2591223 B1 EP2591223 B1 EP 2591223B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- core
- cylinder
- casting
- salt
- slide
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 238000005266 casting Methods 0.000 title claims description 34
- 238000004519 manufacturing process Methods 0.000 title claims description 4
- 150000003839 salts Chemical group 0.000 claims description 32
- 238000000034 method Methods 0.000 claims description 24
- 238000004512 die casting Methods 0.000 claims description 11
- WCUXLLCKKVVCTQ-UHFFFAOYSA-M Potassium chloride Chemical compound [Cl-].[K+] WCUXLLCKKVVCTQ-UHFFFAOYSA-M 0.000 claims description 8
- FAPWRFPIFSIZLT-UHFFFAOYSA-M Sodium chloride Chemical compound [Na+].[Cl-] FAPWRFPIFSIZLT-UHFFFAOYSA-M 0.000 claims description 8
- 229910000831 Steel Inorganic materials 0.000 claims description 8
- 239000000463 material Substances 0.000 claims description 8
- 239000010959 steel Substances 0.000 claims description 8
- 235000011164 potassium chloride Nutrition 0.000 claims description 4
- 239000001103 potassium chloride Substances 0.000 claims description 4
- 239000011780 sodium chloride Substances 0.000 claims description 4
- 229910000838 Al alloy Inorganic materials 0.000 claims description 3
- 238000001746 injection moulding Methods 0.000 claims description 3
- BVKZGUZCCUSVTD-UHFFFAOYSA-L Carbonate Chemical compound [O-]C([O-])=O BVKZGUZCCUSVTD-UHFFFAOYSA-L 0.000 claims 4
- 239000003513 alkali Substances 0.000 claims 4
- 239000000470 constituent Substances 0.000 claims 1
- 238000011010 flushing procedure Methods 0.000 claims 1
- 238000002485 combustion reaction Methods 0.000 description 12
- 239000000203 mixture Substances 0.000 description 4
- 238000000465 moulding Methods 0.000 description 4
- 239000002585 base Substances 0.000 description 3
- 229910052782 aluminium Inorganic materials 0.000 description 2
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 2
- 239000011230 binding agent Substances 0.000 description 2
- 239000000567 combustion gas Substances 0.000 description 2
- 229920002522 Wood fibre Polymers 0.000 description 1
- 229910000288 alkali metal carbonate Inorganic materials 0.000 description 1
- 150000008041 alkali metal carbonates Chemical class 0.000 description 1
- 229910052784 alkaline earth metal Inorganic materials 0.000 description 1
- -1 alkaline earth metal carbonate Chemical class 0.000 description 1
- 229910045601 alloy Inorganic materials 0.000 description 1
- 239000000956 alloy Substances 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 238000007599 discharging Methods 0.000 description 1
- 230000005484 gravity Effects 0.000 description 1
- 239000007769 metal material Substances 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 238000005245 sintering Methods 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 239000002025 wood fiber Substances 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/10—Cores; Manufacture or installation of cores
- B22C9/103—Multipart cores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C1/00—Compositions of refractory mould or core materials; Grain structures thereof; Chemical or physical features in the formation or manufacture of moulds
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/10—Cores; Manufacture or installation of cores
- B22C9/105—Salt cores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/10—Cores; Manufacture or installation of cores
- B22C9/108—Installation of cores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/22—Moulds for peculiarly-shaped castings
- B22C9/24—Moulds for peculiarly-shaped castings for hollow articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D15/00—Casting using a mould or core of which a part significant to the process is of high thermal conductivity, e.g. chill casting; Moulds or accessories specially adapted therefor
- B22D15/02—Casting using a mould or core of which a part significant to the process is of high thermal conductivity, e.g. chill casting; Moulds or accessories specially adapted therefor of cylinders, pistons, bearing shells or like thin-walled objects
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D17/00—Pressure die casting or injection die casting, i.e. casting in which the metal is forced into a mould under high pressure
- B22D17/20—Accessories: Details
- B22D17/22—Dies; Die plates; Die supports; Cooling equipment for dies; Accessories for loosening and ejecting castings from dies
- B22D17/24—Accessories for locating and holding cores or inserts
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D19/00—Casting in, on, or around objects which form part of the product
- B22D19/0009—Cylinders, pistons
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D21/00—Casting non-ferrous metals or metallic compounds so far as their metallurgical properties are of importance for the casting procedure; Selection of compositions therefor
- B22D21/002—Castings of light metals
- B22D21/007—Castings of light metals with low melting point, e.g. Al 659 degrees C, Mg 650 degrees C
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D25/00—Special casting characterised by the nature of the product
- B22D25/02—Special casting characterised by the nature of the product by its peculiarity of shape; of works of art
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F1/00—Cylinders; Cylinder heads
- F02F1/18—Other cylinders
- F02F1/22—Other cylinders characterised by having ports in cylinder wall for scavenging or charging
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02B—INTERNAL-COMBUSTION PISTON ENGINES; COMBUSTION ENGINES IN GENERAL
- F02B75/00—Other engines
- F02B75/02—Engines characterised by their cycles, e.g. six-stroke
- F02B2075/022—Engines characterised by their cycles, e.g. six-stroke having less than six strokes per cycle
- F02B2075/025—Engines characterised by their cycles, e.g. six-stroke having less than six strokes per cycle two
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F2200/00—Manufacturing
- F02F2200/06—Casting
Definitions
- the present invention relates to a method for producing a cylinder for a two-stroke engine and a casting core for this method.
- Such cylinders are typically cast from an aluminum alloy in a gravity casting process using sand cores.
- the problem here is that form very easily casting defects and inclusions. Therefore, it is desirable to cast such cylinders in a die-casting process.
- Sand cores can not be used for this because they do not withstand the pressure conditions prevailing during casting.
- the DE 33 31 664 A1 describes a cylinder with closed Kochströmkanälen for a two-stroke engine, which is produced by die-casting. To form the overflow channels divided steel cores are used, which are connected to the central core valve for the cylinder chamber. Both the design of the multi-part cores and the distance of the split steel cores for the overflow from the cast cylinder make very complex and cumbersome.
- the object of the present invention is to develop a generic method or a generic casting core so that the casting core can be easily removed from the cast cylinder and is nevertheless suitable for a die-casting process.
- the solution is that first a casting core is produced, wherein a central core slide for the cylinder space and at least one salt core for a transfer channel is made and the at least one salt core is connected to the central core slider, that the Gusskem then introduced into a mold and the Cylinder is poured in a die-casting process, then that the central core slider is removed from the cylinder, wherein the at least one salt core is separated from the central core slider and finally the at least one salt core is flushed out of the cylinder.
- the casting core according to the invention is characterized in that it has a central core slide for the cylinder chamber, to which at least one salt core is connected for an overflow channel.
- a salt core connected to a central core slide is so stable that it can withstand the conditions, in particular the pressure conditions, of a die casting process.
- the at least one salt core can be particularly easily flushed out of the cast cylinder in a conventional manner.
- the method according to the invention or the cast core according to the invention thus make it possible to produce cylinders for two-stroke engines which have at least one overflow channel with little outlay in the die casting method.
- the at least one salt core can be produced in a manner known per se by pressing, by injection molding or by sintering.
- Suitable main components are, for example, sodium chloride and / or potassium chloride.
- at least one binder can be added, for example at least one alkali metal carbonate and / or at least one alkaline earth metal carbonate.
- the central core slider can be made of any materials. Preference is given to metallic materials, in particular steel materials.
- the at least one salt core is preferably connected in a form-fitting manner and without binders to the central core slider.
- inventive method or the casting core according to the invention are particularly suitable for the production of cylinders which are cast in a die-casting process from an aluminum alloy.
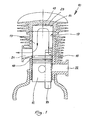
- FIG. 1 shows a schematic representation of a cylinder 10 for a two-stroke engine.
- a piston edge-controlled two-stroke engine is shown, as used, for example, for hand tools such as chainsaws.
- Such a two-stroke engine has at least one cylinder 10 with a cylinder chamber 11, in which a piston 12, which has a piston head 16, is guided movable up and down.
- the cylinder 10 is closed at one end by a cylinder head 13.
- the other end of the cylinder 10 is attached to a crankcase 14, which in FIG. 1 only hinted at.
- the piston 12 is connected by means of a piston pin and a connecting rod with a crankshaft which is rotatably mounted in the crankcase 14 (not shown).
- a combustion chamber 15 is formed, which is bounded by the cylinder head 13, the piston head 16 of the piston 12 and the cylinder wall 17 of the cylinder chamber 11.
- an overflow channel 18 is shown, which connects the combustion chamber 15 with the crankcase 14.
- the cylinder chamber 11 also has an outlet channel 21 for discharging the resulting combustion gases from the combustion chamber 15.
- Below the junction of the overflow channel 18 into the combustion chamber 15, the cylinder chamber 11 also has an inlet channel 22, via which a fuel-air mixture is introduced into the crankcase 14.
- the outlet channel 21, the inlet channel 22 and the junction of the overflow into the combustion chamber 15 are opened and closed by the reciprocating piston 12 in response to its stroke position.
- the piston 12 compresses on its way to top dead center in the combustion chamber 15th During the subsequent downward stroke of the inlet channel 22 is closed and compressed into the crankcase 14 sucked fresh fuel-air mixture. Then first the outlet channel 22 and then the mouth of the overflow 18 are opened into the combustion chamber 15, and the cycle begins again.
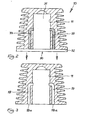
- FIGS. 2 and 3 show an embodiment of the present invention in a simplified representation.
- FIG. 2 shows a cylinder 10 for a two-stroke engine made of an aluminum casting alloy.
- the cylinder 10 was cast in a conventional manner in a die-casting process.
- the casting core 30 used according to the invention has a central core slide 31 and a foot plate 32 provided thereon.
- the core slide 31 serves to form the cylinder space 11.
- the foot plate 32 essentially serves to close the casting mold and, after casting, pull the core slide 31 out of the cast cylinder 10 in the direction of the arrows A.
- the core slide 31 and the base plate 32 are made in the embodiment of the steel material X37CrMoV5-1 cured to 48-52 HRC.
- two salt cores 33 are connected to the core slide 31, which serve to form two overflow channels 18,19.
- the salt cores 33 are in the embodiment of pressed sodium chloride or pressed potassium chloride.
- connection of the salt cores 33 to the core slide by means of a positive connection.
- the Salzkeme 33 are based in the embodiment of the base plate 32 from.
- the finished casting core 30 is inserted into a casting mold.
- the cylinder 10 is cast from an aluminum material in a die casting process.
- the salt cores 33 When pulling out the Kemschiebers 31 after casting of the cylinder 10, the salt cores 33 are sheared off from the core slide 31 and separated from the base plate 32. The salt cores 33 are then flushed out of the cylinder 10 in a manner known per se, so that two overflow channels 18, 19 result.
- the support of the salt cores 33 on the base plate 32 causes the overflow channels in the direction of the later to be added crankcase each having an opening 18 a, 19 a. After adding the crankcase, the transfer ports open into the crankcase.
- FIGS. 4 to 7 show a further embodiment of a cylinder 110 produced by the method according to the invention and a casting core 130 used therefor.
- the cylinder 110 has a cylinder chamber 111, two overflow channels 118, 119, an outlet channel 121 and an inlet channel 122.
- the Gusskem 130 has to form the cylinder space 111 a core slide 131 made of a steel material, in particular made of hot-work steel X37CrMoV5-1 cured to 48-52 HRC.
- Two core cores 133 for forming the overflow channels 118, 119 are connected to the core slide 131.
- a molding 121a for molding an exhaust passage 121 and a molding 122a for molding an intake passage 122 are provided at the central core spool 131.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Materials Engineering (AREA)
- Combustion & Propulsion (AREA)
- General Engineering & Computer Science (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
- Cylinder Crankcases Of Internal Combustion Engines (AREA)
Description
- Die vorliegende Erfindung betrifft ein Verfahren zur Herstellung eines Zylinders für einen Zweitaktmotor sowie einen Gusskern für dieses Verfahren.
- Derartige Zylinder werden in der Regel aus einer Aluminiumlegierung in einem Schwerkraftgussverfahren unter Verwendung von Sandkernen gegossen. Problematisch hierbei ist, dass sich sehr leicht Gießfehler und Einschlüsse bilden. Daher wird angestrebt, derartige Zylinder in einem Druckgussverfahren zu gießen. Hierfür können allerdings keine Sandkerne verwendet werden, da sie den beim Gießen herrschenden Druckverhältnissen nicht standhalten.
- Die
DE 33 31 664 A1 beschreibt einen Zylinder mit geschlossenen Überströmkanälen für einen Zweitaktmotor, der im Druckgussverfahren hergestellt wird. Zu Ausformung der Überströmkanäle werden geteilte Stahlkerne verwendet, die mit dem zentralen Kernschieber für den Zylinderraum verbunden sind. Sowohl die Ausgestaltung der mehrteiligen Kerne als auch die Entfernung der geteilten Stahlkerne für die Überströmkanäle aus dem gegossenen Zylinder gestalten sich sehr aufwändig und umständlich. - Es ist ferner bekannt, Kerne aus einem Holzfasermaterial zu verwenden (vgl.
DE 198 20 246 A1 ). Derartige Kerne haben sich für das Druckgussverfahren jedoch nicht bewährt, da sie hierfür nicht stabil genug sind. - Die Aufgabe der vorliegenden Erfindung besteht darin, ein gattungsgemäßes Verfahren bzw. einen gattungsgemäßen Gusskern so weiterzuentwickeln, dass der Gusskern leicht aus dem gegossenen Zylinder entfernt werden kann und gleichwohl für ein Druckgussverfahren geeignet ist.
- Die Lösung besteht darin, dass zunächst ein Gusskern hergestellt wird, wobei ein zentraler Kernschieber für den Zylinderraum und mindestens ein Salzkern für einen Überströmkanal hergestellt wird und der mindestens eine Salzkern an den zentralen Kernschieber angebunden wird, dass der Gusskem anschließend in eine Gießform eingebracht und der Zylinder in einem Druckgussverfahren gegossen wird, dass anschließend der zentrale Kernschieber aus dem Zylinder entfernt wird, wobei der mindestens eine Salzkern vom zentralen Kernschieber abgetrennt wird und schließlich der mindestens eine Salzkern aus dem Zylinder ausgespült wird.
- Der erfindungsgemäße Gusskern zeichnet sich dadurch aus, dass er einen zentralen Kernschieber für den Zylinderraum aufweist, an den mindestens ein Salzkern für einen Überströmkanal angebunden ist.
- Für den Fachmann überraschend hat sich herausgestellt, dass ein an einen zentralen Kernschieber angebundener Salzkern so stabil ist, dass er den Bedingungen, insbesondere den Druckverhältnissen, eines Druckgussverfahrens standhält. Der mindestens eine Salzkern kann in an sich bekannter Weise besonders einfach aus dem gegossenen Zylinder ausgespült werden. Das erfindungsgemäße Verfahren bzw. der erfindungsgemäße Gusskern erlauben es also, Zylinder für Zweitaktmotoren, die mindestens einen Überströmkanal aufweisen, mit geringem Aufwand im Druckgussverfahren herzustellen.
- Vorteilhafte Weiterbildungen ergeben sich aus den Unteransprüchen.
- Der mindestens eine Salzkern kann in an sich bekannter Weise durch Pressen, durch Spritzgießen oder durch Sintern hergestellt werden. Als Hauptbestandteile eignen sich bspw. Natriumchlorid und/oder Kaliumchlorid. Bei Bedarf kann mindestens ein Bindemittel hingefügt werden, bspw. mindestens ein Alkalicarbonat und/oder mindestens ein Erdalkalicarbonat.
- Der zentrale Kernschieber kann aus beliebigen Werkstoffen hergestellt werden. Bevorzugt sind metallische Werkstoffe, insbesondere Stahlwerkstoffe.
- Der mindestens eine Salzkern wird bevorzugt formschlüssig und ohne Bindemittel an den zentralen Kernschieber angebunden.
- Das erfindungsgemäße Verfahren bzw. der erfindungsgemäße Gusskern eignen sich insbesondere zur Herstellung von Zylindern, die in einem Druckgussverfahren aus einer Aluminiumlegierung gegossen werden.
- Ausführungsbeispiele der vorliegenden Erfindung werden im Folgenden anhand der beigefügten Zeichnungen näher erläutert. Es zeigen in einer schematischen, nicht maßstabsgetreuen Darstellung:
- Figur 1
- eine beispielhafte Gesamtdarstellung eines Zylinders für einen Zweitaktmotor im Schnitt;
- Figur 2
- einen Zylinder für einen Zweitaktmotor mit einem darin befindlichen ersten Ausführungsbeispiel eines erfindungsgemäßen Gusskerns im Schnitt;
- Figur 3
- den Zylinder gemäß
Figur 1 nach Entfernen des Gusskerns; - Figur 4
- ein weiteres Ausführungsbeispiel eines erfindungsgemäßen Gusskerns in einer perspektivischen Schrägansicht;
- Figur 5
- den Gusskern gemäß
Figur 4 in einer Frontansicht; - Figur 6
- einen weiteren Zylinder für einen Zweitaktmotor im Schnitt, hergestellt mit einem Gusskem gemäß den
Figuren 4 und 5 ; - Figur 7
- einen Schnitt entlang der Linie VII - VII in
Figur 6 . -
Figur 1 zeigt eine schematische Darstellung eines Zylinders 10 für einen Zweitaktmotor. Im Ausführungsbeispiel ist ein kolbenkantengesteuerter Zweitaktmotor dargestellt, wie er bspw. für Handwerkzeuge wie Motorsägen verwendet wird. Ein solcher Zweitaktmotor weist mindestens einen Zylinder 10 mit einem Zylinderraum 11, in dem ein Kolben 12, der einen Kolbenboden 16 aufweist, auf und ab bewegbar geführt ist. Der Zylinder 10 ist an einem Ende von einem Zylinderkopf 13 verschlossen. Das andere Ende des Zylinders 10 ist an einem Kurbelgehäuse 14 befestigt, das inFigur 1 nur andeutungsweise dargestellt ist. In an sich bekannter Weise ist der Kolben 12 mittels eines Kolbenbolzens und eines Pleuels mit einer Kurbelwelle verbunden, die im Kurbelgehäuse 14 drehbar gelagert ist (nicht dargestellt). - Im Zylinder 10 ist ein Brennraum 15 ausgebildet, der vom Zylinderkopf 13, dem Kolbenboden 16 des Kolbens 12 und der Zylinderwand 17 des Zylinderraums 11 begrenzt ist. Im Ausführungsbeispiel ist ein Überströmkanal 18 dargestellt, der den Brennraum 15 mit dem Kurbelgehäuse 14 verbindet. Der Zylinderraum 11 weist ferner einen Auslasskanal 21 zum Abführen der anfallenden Verbrennungsgase aus dem Brennraum 15 auf. Unterhalb der Einmündung des Überströmkanals 18 in den Brennraum 15 weist der Zylinderraum 11 ferner einen Einlasskanal 22 auf, über den ein Brennstoff-Luft-Gemisch in das Kurbelgehäuse 14 eingeleitet wird. Der Auslasskanal 21, der Einlasskanal 22 und die Einmündung des Überströmkanals in den Brennraum 15 werden von dem auf- und abgehenden Kolben 12 in Abhängigkeit seiner Hubstellung geöffnet und geschlossen.
- In der in
Figur 1 dargestellten Stellung des Kolbens 12 im Bereich seines unteren Totpunktes sind der Auslasskanal 21 und die Einmündung des Überströmkanals 18 in den Brennraum 15 geöffnet. In dieser Stellung strömt das vom Kolben 12 im Kurbelgehäuse verdichtete Brennstoff-Luft-Gemisch in den Brennraum 15 (siehe Pfeil S) und verdrängt die Brennraum 15 befindlichen Verbrennungsgase, die über den Auslasskanal 21 aus dem Brennraum 15 austreten. Bei der folgenden Aufwärtsbewegung des Kolbens 12 in Richtung auf den Zylinderkopf 13 wird zunächst die Mündung des Überströmkanals 18 in den Brennraum 15 und anschließend der Auslasskanal 21 verschlossen. Gleichzeitig wird der Einlasskanal 22 geöffnet, so dass frisches Brennstoff-Luft-Gemisch in das Kurbelgehäuse 14 gesaugt wird. Der Kolben 12 verdichtet auf seinem Weg zum oberen Totpunkt das im Brennraum 15 befindliche Brennstoff-Luft-Gemisch bis zur Zündung unterhalb des vom Zylinderkopf 13 gebildeten Brennraumdachs 23. Beim anschließenden Abwärtshub wird der Einlasskanal 22 verschlossen und das in das Kurbelgehäuse 14 gesaugte frische Brennstoff-Luft-Gemisch verdichtet. Dann werden zunächst der Auslasskanal 22 und anschließend die Mündung des Überströmkanals 18 in den Brennraum 15 geöffnet, und der Arbeitszyklus beginnt von neuem. - Die
Figuren 2 und 3 zeigen ein Ausführungsbeispiel der vorliegenden Erfindung in einer vereinfachten Darstellung.Figur 2 zeigt einen Zylinder 10 für einen ZweitaktMotor aus einer Aluminiumgusslegierung. Der Zylinder 10 wurde in an sich bekannter Weise in einem Druckgussverfahren gegossen. - Der hierfür verwendete erfindungsgemäße Gusskern 30 weist einen zentralen Kernschieber 31 und eine daran vorgesehene Fußplatte 32 auf. Der Kernschieber 31 dient zur Ausformung des Zylinderraums 11. Die Fußplatte 32 dient im Wesentlichen dazu, die Gießform zu verschließen und nach dem Gießen den Kernschieber 31 aus dem gegossenen Zylinder 10 in Richtung der Pfeile A herauszuziehen. Der Kernschieber 31 und die Fußplatte 32 bestehen im Ausführungsbeispiel aus dem Stahlwerkstoff X37CrMoV5-1 gehärtet auf 48-52 HRC.
- Im Ausführungsbeispiel sind an den Kernschieber 31 zwei Salzkerne 33 angebunden, die zur Ausformung zweier Überströmkanäle 18,19 dienen. Die Salzkerne 33 bestehen im Ausführungsbeispiel aus gepresstem Natriumchlorid oder aus gepresstem Kaliumchlorid.
- Die Anbindung der Salzkerne 33 an den Kernschieber erfolgt mittels einer formschlüssigen Verbindung.
- Die Salzkeme 33 stützen sich im Ausführungsbeispiel auf der Fußplatte 32 ab. Der fertige Gusskern 30 wird in eine Gießform eingelegt. Der Zylinder 10 wird aus einem Aluminiumwerkstoff in einem Druckgussverfahren gegossen.
- Beim Herausziehen des Kemschiebers 31 nach dem Gießen des Zylinders 10 werden die Salzkerne 33 vom Kernschieber 31 abgeschert bzw. von der Fußplatte 32 abgetrennt. Die Salzkerne 33 werden nun in an sich bekannter Weise aus dem Zylinder 10 ausgespült, so dass zwei Überströmkanäle 18, 19 resultieren. Die Abstützung der Salzkerne 33 auf der Fußplatte 32 bewirkt, dass die Überströmkanäle in Richtung des später hinzuzufügenden Kurbelgehäuses jeweils eine Öffnung 18a, 19a aufweisen. Nach dem Hinzufügen des Kurbelgehäuses münden die Überströmkanäle in das Kurbelgehäuse.
- Die
Figuren 4 bis 7 zeigen ein weiteres Ausführungsbeispiel eines nach dem erfindungsgemäßen Verfahren hergestellten Zylinders 110 und eines hierfür verwendeten Gusskerns 130. Der Zylinder 110 weist einen Zylinderraum 111, zwei Überströmkanäle 118, 119, einen Auslasskanal 121 und einen Einlasskanal 122 auf. Der Gusskem 130 weist zur Ausformung des Zylinderraums 111 einen Kernschieber 131 aus einem Stahlwerkstoff, insbesondere aus Warmarbeitsstahl X37CrMoV5-1 gehärtet auf 48-52 HRC auf. An den Kernschieber 131 sind zwei Salzkerne 133 zur Ausformung der Überströmkanäle 118, 119 angebunden. Ferner sind ein Formteil 121a zur Ausformung eines Auslasskanals 121 und ein Formteil 122a zur Ausformung eines Einlasskanals 122 am zentralen Kernschieber 131 vorgesehen.
Claims (17)
- Verfahren zur Herstellung eines Zylinders (10, 110) für einen Zweitakt-Motor, mit den folgenden Verfahrensschritten:- Herstellen eines Gusskerns (30, 130), wobei ein zentraler Kernschieber (31, 131) für den Zylinderraum (11, 111) und mindestens ein Salzkern (33, 133) für einen Überströmkanal (18, 19; 118, 119) hergestellt wird und der mindestens eine Salzkern (33, 133) an den zentralen Kernschieber (31, 131) angebunden wird,- Einbringen des Gusskerns (30, 130) in eine Gießform,- Gießen des Zylinders (10, 110) in einem Druckgussverfahren,- Entfernen des zentralen Kemschiebers (31, 131) aus dem Zylinder (10, 110), wobei der mindestens eine Salzkern (33, 133) vom zentralen Kernschieber (31, 131) abgetrennt wird,- Ausspülen des mindestens einen Salzkerns (33, 133) aus dem Zylinder (10,110).
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) gepresst wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) gesintert wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) im Spritzgussverfahren hergestellt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) aus Natriumchlorid als Hauptbestandteil hergestellt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) aus Kaliumchlorid als Hauptbestandteil hergestellt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) unter Verwendung mindestens eines Alkalicarbonats und/oder mindestens eines Erdalkalicarbonats hergestellt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der zentrale Kernschieber (31, 131) aus einem Stahlwerkstoff hergestellt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der Zylinder (10, 110) aus einer Aluminiumlegierung gegossen wird.
- Gusskem (30, 130) zur Herstellung eines Zylinders (10, 110) für einen Zweitakt-Motor, mit einem zentralen Kernschieber (31, 131) für den Zylinderraum (11, 111), dadurch gekennzeichnet, dass an den zentralen Kernschieber (31, 131) mindestens ein Salzkern (33, 133) für einen Überströmkanal (18, 19; 118, 119) angebunden ist.
- Gusskem nach Anspruch 10, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) gepresst ist.
- Gusskem nach Anspruch 10, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) gesintert ist.
- Gusskem nach Anspruch 10, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) im Spritzgussverfahren hergestellt ist.
- Gusskem nach Anspruch 10, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) aus Natriumchlorid als Hauptbestandteil besteht.
- Gusskem nach Anspruch 10, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) aus Kaliumchlorid als Hauptbestandteil besteht.
- Gusskem nach Anspruch 10, dadurch gekennzeichnet, dass der mindestens eine Salzkern (33, 133) mindestens ein Alkalicarbonat und/oder mindestens ein Erdalkalicarbonat enthält.
- Gusskem nach Anspruch 10, dadurch gekennzeichnet, dass der zentrale Kernschieber (31, 131) aus einem Stahlwerkstoff besteht.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102010026597A DE102010026597A1 (de) | 2010-07-08 | 2010-07-08 | Verfahren zur Herstellung eines Zylinders für einen Zweitaktmotor sowie Gusskern hierfür |
| PCT/DE2011/001408 WO2012010144A2 (de) | 2010-07-08 | 2011-07-05 | Verfahren zur herstellung eines zylinders für einen zweitaktmotor sowie gusskern hierfür |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2591223A2 EP2591223A2 (de) | 2013-05-15 |
| EP2591223B1 true EP2591223B1 (de) | 2015-03-18 |
Family
ID=45372440
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP11808135.5A Not-in-force EP2591223B1 (de) | 2010-07-08 | 2011-07-05 | Verfahren zur herstellung eines zylinders für einen zweitaktmotor sowie gusskern hierfür |
Country Status (5)
| Country | Link |
|---|---|
| US (2) | US20130264022A1 (de) |
| EP (1) | EP2591223B1 (de) |
| CN (1) | CN102985675B (de) |
| DE (1) | DE102010026597A1 (de) |
| WO (1) | WO2012010144A2 (de) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015216452A1 (de) * | 2015-08-27 | 2017-03-16 | Volkswagen Aktiengesellschaft | Werkzeug und Kokillengießverfahren zur Herstellung eines Zylinderkurbelgehäuses |
| DE102015216224A8 (de) * | 2015-08-25 | 2017-06-29 | Volkswagen Aktiengesellschaft | Gussform mit integrierten Kernlagerbolzen und Verfahren zur Herstellung eines Gussbauteils |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102011079356A1 (de) * | 2011-07-18 | 2013-01-24 | Mahle International Gmbh | Gießkern einer Gussform zur Herstellung eines Zylinders |
| DE102017205853A1 (de) * | 2017-04-06 | 2018-10-11 | Bayerische Motoren Werke Aktiengesellschaft | Kernpaket |
| WO2021101102A1 (ko) * | 2019-11-21 | 2021-05-27 | 주식회사 평화발레오 | 마스터 실린더 제조방법 |
Family Cites Families (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1465486A (en) * | 1973-04-18 | 1977-02-23 | Aeroplane Motor Alu Cast | Method and apparatus for forming a curved passage in a casting and a casting so formed |
| US4003422A (en) * | 1975-04-21 | 1977-01-18 | Schramm Buford J | Process for making a composite cylinder head assembly |
| US4252175A (en) * | 1979-05-25 | 1981-02-24 | Outboard Marine Corporation | Cylinder block having a cast-in core unit and process for manufacturing same |
| US4446906A (en) * | 1980-11-13 | 1984-05-08 | Ford Motor Company | Method of making a cast aluminum based engine block |
| DE3331664A1 (de) | 1983-09-02 | 1985-03-21 | Fichtel & Sachs Ag, 8720 Schweinfurt | Zylinder fuer hubkolben-brennkraftmaschine, insbesondere zweitakt-brennkraftmaschine |
| JP2797187B2 (ja) * | 1988-06-06 | 1998-09-17 | 本田技研工業株式会社 | 2サイクルエンジン用シリンダブロックの鋳造方法 |
| JP3747115B2 (ja) | 1997-05-16 | 2006-02-22 | 株式会社共立 | ダイカスト鋳造用中子 |
| US6527039B2 (en) * | 2001-06-11 | 2003-03-04 | General Motors Corporation | Casting of engine blocks |
| ITBS20020088A1 (it) * | 2002-10-04 | 2004-04-05 | Meccanica Bassi Spa | Procedimento di fusione, in particolare per testa cilindri di motori |
| DE102006001946B8 (de) * | 2006-01-14 | 2010-06-02 | Audi Ag | Zylinderbuchseneinlegeteil für ein Zylindergehäuse einer Hubkolben-Brennkraftmaschine und Verfahren zur Herstellung eines solchen Zylinderbuchseneinlegeteils |
| DE102007014146A1 (de) * | 2007-03-23 | 2007-11-22 | Daimlerchrysler Ag | Druckgießwerkzeug |
| DE102007023060A1 (de) * | 2007-05-16 | 2008-11-20 | Daimler Ag | Verfahren zur Herstellung eines Zylinderkurbelgehäuses |
| CN201081012Y (zh) * | 2007-09-05 | 2008-07-02 | 山东滨州渤海活塞股份有限公司 | 异型内冷油腔结构活塞 |
| CN101391280B (zh) * | 2007-09-18 | 2011-02-09 | 山东滨州渤海活塞股份有限公司 | 压力铸造用异型盐芯 |
-
2010
- 2010-07-08 DE DE102010026597A patent/DE102010026597A1/de not_active Withdrawn
-
2011
- 2011-07-05 EP EP11808135.5A patent/EP2591223B1/de not_active Not-in-force
- 2011-07-05 US US13/808,702 patent/US20130264022A1/en not_active Abandoned
- 2011-07-05 WO PCT/DE2011/001408 patent/WO2012010144A2/de not_active Ceased
- 2011-07-05 CN CN201180033482.5A patent/CN102985675B/zh not_active Expired - Fee Related
-
2015
- 2015-12-01 US US14/955,303 patent/US20160089716A1/en not_active Abandoned
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015216224A8 (de) * | 2015-08-25 | 2017-06-29 | Volkswagen Aktiengesellschaft | Gussform mit integrierten Kernlagerbolzen und Verfahren zur Herstellung eines Gussbauteils |
| DE102015216452A1 (de) * | 2015-08-27 | 2017-03-16 | Volkswagen Aktiengesellschaft | Werkzeug und Kokillengießverfahren zur Herstellung eines Zylinderkurbelgehäuses |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2591223A2 (de) | 2013-05-15 |
| US20130264022A1 (en) | 2013-10-10 |
| US20160089716A1 (en) | 2016-03-31 |
| WO2012010144A3 (de) | 2012-06-07 |
| CN102985675A (zh) | 2013-03-20 |
| WO2012010144A2 (de) | 2012-01-26 |
| CN102985675B (zh) | 2016-04-27 |
| DE102010026597A1 (de) | 2012-01-12 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| WO2012010144A2 (de) | Verfahren zur herstellung eines zylinders für einen zweitaktmotor sowie gusskern hierfür | |
| DE2927239A1 (de) | Kokillengussmaschine zur herstellung waermebestaendiger laeufer | |
| DE2308127B2 (de) | Zweitakt-Brennkraftmaschine mit zwei bzw. drei Kompressionsräumen | |
| DE2727979B2 (de) | Vorrichtung zur Einspritzung von Wasser in die Zylinder einer Brennkraftmaschine | |
| EP2129480A1 (de) | Druckgiesswerkzeuganordnung | |
| DE10041547A1 (de) | Zweitaktmotor mit belüftetem Überströmkanal | |
| DE102011110176B4 (de) | Druckgießmaschine sowie Druckgießverfahren | |
| EP0933151B1 (de) | Giessform und Verfahren zum Herstellen von Gussstücken | |
| DE19807568C2 (de) | Druckgußmaschine | |
| DE102017109716B3 (de) | Metall-Druckguss-Formwerkzeug | |
| DE532218C (de) | Steinpresse, deren Beschicker und Entlader durch eine Kurbel, Kurvenscheibe o. dgl. angetrieben werden | |
| EP1498197A1 (de) | Verfahren zum Giessen von Kurbelgehäusen für Hubkolbenbrennkraftmaschinen | |
| EP2644862B1 (de) | Brennkraftmaschine, insbesondere 2-Takt-Brennkraftmaschine | |
| DE102006045729A1 (de) | Kolben für einen Verbrennungsmotor und Verfahren zu seiner Herstellung | |
| DE651029C (de) | Metallbarren fuer die Weiterverarbeitung durch Kneten | |
| EP1486750A1 (de) | Verschluss für eine Faustfeuerwaffe | |
| DE3431851C1 (de) | Gießmaschine zum Gießen von Kolben | |
| DE361145C (de) | Barrenpresse | |
| DE496315C (de) | Pressgussmaschine mit durch Federn beeinflussten Formstuecken | |
| DE584464C (de) | Maschine zur Herstellung der Anoden von Trockenbatterien | |
| AT121709B (de) | Vorrichtung zum Gießen der Läuferstäbe von Kurzschlußläufermotoren. | |
| DE844064C (de) | Vorrichtung zum Pressen grosser Teile aus haertbarer Kunstharzmasse im Fliessverfahren | |
| DE201159C (de) | ||
| DE2402787A1 (de) | Vorrichtung zum formen von hohlkammern aufweisenden formsteinen | |
| DE23944C (de) | Presse zur Formung von schlesischen Zinkmuffeln etc |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20130208 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20141013 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 716749 Country of ref document: AT Kind code of ref document: T Effective date: 20150415 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502011006343 Country of ref document: DE Effective date: 20150430 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20150318 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20150318 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150618 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150619 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150720 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150718 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502011006343 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| 26N | No opposition filed |
Effective date: 20151221 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150705 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150731 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150731 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150705 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20110705 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 716749 Country of ref document: AT Kind code of ref document: T Effective date: 20160705 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160705 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150318 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20230720 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20230725 Year of fee payment: 13 Ref country code: DE Payment date: 20230719 Year of fee payment: 13 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20240527 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502011006343 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20240705 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240705 |