EP0988664B1 - Elektrische steckverbindung - Google Patents
Elektrische steckverbindung Download PDFInfo
- Publication number
- EP0988664B1 EP0988664B1 EP98930696A EP98930696A EP0988664B1 EP 0988664 B1 EP0988664 B1 EP 0988664B1 EP 98930696 A EP98930696 A EP 98930696A EP 98930696 A EP98930696 A EP 98930696A EP 0988664 B1 EP0988664 B1 EP 0988664B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- connection
- integral
- contact
- mating contact
- plug
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images
Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01R—ELECTRICALLY-CONDUCTIVE CONNECTIONS; STRUCTURAL ASSOCIATIONS OF A PLURALITY OF MUTUALLY-INSULATED ELECTRICAL CONNECTING ELEMENTS; COUPLING DEVICES; CURRENT COLLECTORS
- H01R4/00—Electrically-conductive connections between two or more conductive members in direct contact, i.e. touching one another; Means for effecting or maintaining such contact; Electrically-conductive connections having two or more spaced connecting locations for conductors and using contact members penetrating insulation
- H01R4/02—Soldered or welded connections
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01R—ELECTRICALLY-CONDUCTIVE CONNECTIONS; STRUCTURAL ASSOCIATIONS OF A PLURALITY OF MUTUALLY-INSULATED ELECTRICAL CONNECTING ELEMENTS; COUPLING DEVICES; CURRENT COLLECTORS
- H01R4/00—Electrically-conductive connections between two or more conductive members in direct contact, i.e. touching one another; Means for effecting or maintaining such contact; Electrically-conductive connections having two or more spaced connecting locations for conductors and using contact members penetrating insulation
- H01R4/02—Soldered or welded connections
- H01R4/027—Soldered or welded connections comprising means for positioning or holding the parts to be soldered or welded
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01R—ELECTRICALLY-CONDUCTIVE CONNECTIONS; STRUCTURAL ASSOCIATIONS OF A PLURALITY OF MUTUALLY-INSULATED ELECTRICAL CONNECTING ELEMENTS; COUPLING DEVICES; CURRENT COLLECTORS
- H01R43/00—Apparatus or processes specially adapted for manufacturing, assembling, maintaining, or repairing of line connectors or current collectors or for joining electric conductors
- H01R43/02—Apparatus or processes specially adapted for manufacturing, assembling, maintaining, or repairing of line connectors or current collectors or for joining electric conductors for soldered or welded connections
- H01R43/0221—Laser welding
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49002—Electrical device making
- Y10T29/49117—Conductor or circuit manufacturing
- Y10T29/49124—On flat or curved insulated base, e.g., printed circuit, etc.
- Y10T29/4913—Assembling to base an electrical component, e.g., capacitor, etc.
- Y10T29/49139—Assembling to base an electrical component, e.g., capacitor, etc. by inserting component lead or terminal into base aperture
- Y10T29/4914—Assembling to base an electrical component, e.g., capacitor, etc. by inserting component lead or terminal into base aperture with deforming of lead or terminal
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49002—Electrical device making
- Y10T29/49117—Conductor or circuit manufacturing
- Y10T29/49124—On flat or curved insulated base, e.g., printed circuit, etc.
- Y10T29/4913—Assembling to base an electrical component, e.g., capacitor, etc.
- Y10T29/49139—Assembling to base an electrical component, e.g., capacitor, etc. by inserting component lead or terminal into base aperture
- Y10T29/4914—Assembling to base an electrical component, e.g., capacitor, etc. by inserting component lead or terminal into base aperture with deforming of lead or terminal
- Y10T29/49142—Assembling to base an electrical component, e.g., capacitor, etc. by inserting component lead or terminal into base aperture with deforming of lead or terminal including metal fusion
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49002—Electrical device making
- Y10T29/49117—Conductor or circuit manufacturing
- Y10T29/49124—On flat or curved insulated base, e.g., printed circuit, etc.
- Y10T29/4913—Assembling to base an electrical component, e.g., capacitor, etc.
- Y10T29/49144—Assembling to base an electrical component, e.g., capacitor, etc. by metal fusion
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49002—Electrical device making
- Y10T29/49117—Conductor or circuit manufacturing
- Y10T29/49174—Assembling terminal to elongated conductor
- Y10T29/49179—Assembling terminal to elongated conductor by metal fusion bonding
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49002—Electrical device making
- Y10T29/49117—Conductor or circuit manufacturing
- Y10T29/49174—Assembling terminal to elongated conductor
- Y10T29/49181—Assembling terminal to elongated conductor by deforming
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49002—Electrical device making
- Y10T29/49117—Conductor or circuit manufacturing
- Y10T29/49204—Contact or terminal manufacturing
- Y10T29/49208—Contact or terminal manufacturing by assembling plural parts
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49002—Electrical device making
- Y10T29/49117—Conductor or circuit manufacturing
- Y10T29/49204—Contact or terminal manufacturing
- Y10T29/49208—Contact or terminal manufacturing by assembling plural parts
- Y10T29/4921—Contact or terminal manufacturing by assembling plural parts with bonding
- Y10T29/49211—Contact or terminal manufacturing by assembling plural parts with bonding of fused material
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/53—Means to assemble or disassemble
- Y10T29/5313—Means to assemble electrical device
- Y10T29/532—Conductor
- Y10T29/53209—Terminal or connector
Definitions
- the invention relates to a method and a device for producing an electrical Connection according to the characteristics of the respective generic term of the independent Claims.
- the invention is therefore based on the object of a method and a device to establish an electrical connection with which the electrical Connection can not only be made easy to assemble, but above it also offers maximum contact security.
- the invention is therefore based on the basic idea of an initially solvable one Connection with the advantage of simple, precise, reverse polarity protected and Modify quick installation friendliness so that after the modification (integral or quasi-integral connection) cannot be removed to ensure a high level of contact security.
- This also has the advantage that the process is automated particularly in the context of series production leaves.
- the quasi-integral connection is produced by crimping or clamping connections. Such a connection comes into consideration especially if the two contact partners are free accessible and not surrounded by a housing.
- the one contact partner becomes a contact guide inserted in the area of the other contact partner in a connector housing and through an opening in the connector housing the integral or the quasi-integral Connected.
- the cohesive or the quasi-cohesive Connection established within this component group or the housing thereby it is possible within a component group or within a housing several modules, components or the like by merging of the two contact partners to be electrically connected to one another as a plug connection and then within this component group the cohesive or establish the quasi-integral connection.
- the cohesive or establish the quasi-integral connection is also comes into consideration that not only modules or components be connected within this component group, but that also feeds from outside or outside can be connected to one or more modules. Thereby there is no need for cumbersome assembly of pre-assembled ones and electrically connected modules that are cumbersome in the Housing would have to be used.
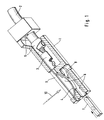
- Figure 1 shows a preferred embodiment of an inventive electrical connection, to which the general idea of the invention, however is not limited.
- Reference number 1 denotes a connector housing, on one of which There is a cable 2 at the end. Inside the connector housing 1 is a first contact partner 3 (for example plug or socket) is arranged, wherein the first contact partner 3 is designed such that the cable 2, for example by means of a conventional crimp connection on this is attached and in the area facing away from the cable 2 a contact tab 4 has.
- the cable 2 is in a manner known per se via strain reliefs 5 on the contact partner 3 and / or on the connector housing 1 strain relief. This is during the connection process and Also an advantage during operation, because the connection and vibrating load is largely free of forces.
- the connector housing 1 also has a contact guide 6, wherein in this contact 6 a second contact partner 7 (for example socket or connector), which is also connected to a cable, a printed circuit board or the like can be connected, is introduced (indicated by the Arrow in the second contact partner 7).
- the contact guide 6 also serves Reduction of the degrees of freedom (positioning aid) of the second contact partner 7.
- a latching 8 arranged after the introduction of the second Contact partner 7 in the contact guides 6 defines this.
- Such Locking can alternatively also be present on the second contact partner 7 his.
- the plug housing 1 (or a correspondingly designed socket housing) is to include only one contact partner 3 inclusive his associated further contact partner 7 trained. It is of course also conceivable that several contact partners 3 (or 7) next to and / or one above the other and / or in the form of an arc, circle and / or cube are arranged in the connector housing and the associated openings 9 are accessible from the outside. It is also conceivable after having done so Joining process to cover the opening (s) 9.
- the idea according to the invention is basically applicable to electrical Plug connections that are easy to install, Installation speed and high contact reliability are important.
- a special Field of application, to which, however, the invention is not restricted is the field of adjusting devices for adjusting the power of internal combustion engines, commonly referred to as e-gas become.
- the electrical connection and the cables attached to it the power supply to the Servomotor manufactured, but also the position of the throttle valve, for example by means of a throttle valve potentiometer or the like is detected, reported back to a control device.
- the cables for the power supply and for the feedback in introduced the housing of the actuating device and by means of the invention Plug connection the electrical connection to the throttle valve potentiometer or the like and / or made to the servomotor.
Landscapes
- Connections Effected By Soldering, Adhesion, Or Permanent Deformation (AREA)
- Connector Housings Or Holding Contact Members (AREA)
- Manufacturing Of Electrical Connectors (AREA)
- Coupling Device And Connection With Printed Circuit (AREA)
- Details Of Connecting Devices For Male And Female Coupling (AREA)
- Multi-Conductor Connections (AREA)
Description
- 1.
- Steckergehäuse
- 2.
- Kabel
- 3.
- erster Kontaktpartner
- 4.
- Kontaktfahne
- 5.
- Zugentlastung
- 6.
- Kontaktführungen
- 7.
- zweiter Kontaktpartner
- 8.
- Verrastung
- 9.
- Öffnung
- 10.
- Laserstrahl
Claims (11)
- Verfahren zur Herstellung einer elektrischen Verbindung zwischen einem ersten und einem zweiten Kontaktpartner, dadurch gekennzeichnet, dass die beiden Kontaktpartner als Steckverbindung zusammengeführt und anschließend durch eine einzige Öffnung durch Laserschweißen stoffschlüssig oder quasi-stoffschlüssig unlösbar miteinander verbunden werden.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass die quasi-stoffschlüssige Verbindung durch Crimp- oder Klemmverbindungen hergestellt wird.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, dass der eine Kontaktpartner in eine Kontaktführung im Bereich des anderen Kontaktpartners in einem Steckergehäuse eingeführt wird und durch eine Öffnung in dem Steckergehäuse die stoffschlüssige oder die quasi-stoffschlüssige Verbindung hergestellt wird.
- Verfahren nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die stoffschlüssige oder die quasi-stoffschlüssige Verbindung innerhalb einer Bauteilgruppe hergestellt wird.
- Verfahren nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die stoffschlüssige oder die quasi-stoffschlüssige Verbindung hergestellt wird und anschließend in eine Bauteilgruppe eingeführt wird.
- Vorrichtung zur Herstellung einer elektrischen Verbindung zwischen einem ersten Kontaktpartner (3, 4) und einem zweiten Kontaktpartner (7), dadurch gekennzeichnet, dass die beiden Kontaktpartner (3, 4, 7) als Steckverbindung zusammenführbar und anschließend durch eine einzige Öffnung (9) durch Laserschweißen stoffschlüssig oder quasi-stoffschlüssig unlösbar miteinander verbindbar sind.
- Vorrichtung nach Anspruch 6, dadurch gekennzeichnet, dass die Steckverbindung ein den ersten Kontaktpartner (3, 4) aufnehmendes Steckergehäuse (1) mit einer Aufnahmeöffnung zur Einführung des zweiten Kontaktpartner (7) aufweist.
- Vorrichtung nach Anspruch 6 oder 7, dadurch gekennzeichnet, dass die Steckverbindung beziehungsweise das Steckergehäuse (1) eine Öffnung (9) zur Herstellung der stoffschlüssigen oder der quasi-stoffschlüssigen Verbindung aufweist.
- Vorrichtung nach einem der Ansprüche 6 bis 8, dadurch gekennzeichnet, dass mehrere erste Kontaktpartner (3, 4) nebeneinander angeordnet die Steckverbindung bilden.
- Vorrichtung nach einem der Ansprüche 6 bis 9, dadurch gekennzeichnet, dass das Steckergehäuse (1) zumindest eine Verrastung (8) für den zweiten Kontaktpartner (7) aufweist.
- Vorrichtung nach einem der Ansprüche 6 bis 10, dadurch gekennzeichnet, dass die Steckverbindung in oder an einer Bauteilgruppe, insbesondere einem Gehäuse einer Stellvorrichtung zur Einstellung der Leistung einer Brennkraftmaschine [E-Gas], angeordnet ist.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19724336A DE19724336A1 (de) | 1997-06-10 | 1997-06-10 | Steckverbindung |
| DE19724336 | 1997-06-10 | ||
| PCT/EP1998/002901 WO1998057393A1 (de) | 1997-06-10 | 1998-05-16 | Elektrische steckverbindung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0988664A1 EP0988664A1 (de) | 2000-03-29 |
| EP0988664B1 true EP0988664B1 (de) | 2001-11-21 |
Family
ID=7831976
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98930696A Expired - Lifetime EP0988664B1 (de) | 1997-06-10 | 1998-05-16 | Elektrische steckverbindung |
Country Status (10)
| Country | Link |
|---|---|
| US (2) | US20020144398A1 (de) |
| EP (1) | EP0988664B1 (de) |
| JP (1) | JP2002503382A (de) |
| KR (1) | KR100635677B1 (de) |
| AT (1) | ATE209400T1 (de) |
| BR (1) | BR9810425A (de) |
| DE (2) | DE19724336A1 (de) |
| ES (1) | ES2168769T3 (de) |
| MY (1) | MY122253A (de) |
| WO (1) | WO1998057393A1 (de) |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19945946C1 (de) * | 1999-09-24 | 2001-05-31 | Eiv Engeser Innovative Verbind | Verfahren zur Herstellung einer elektrischen Verbindung |
| ATE369031T1 (de) * | 2004-04-08 | 2007-08-15 | Ebm Papst St Georgen Gmbh & Co | Anordnung mit einem kontaktelement |
| DE102004026792B4 (de) * | 2004-06-02 | 2008-12-24 | Continental Automotive Gmbh | Körpervorrichtung |
| DE102004053126A1 (de) * | 2004-11-03 | 2006-05-11 | Tyco Electronics Amp Gmbh | Verfahren und Vorrichtung zur Verbindung eines elektrischen Übertragungselementes mit einem Kontaktelement |
| DE102008022057B4 (de) * | 2008-05-03 | 2010-04-08 | Lumberg Connect Gmbh | Kontakt für eine Anschlussdose und Vefahren zur Herstellung einer Zugentlastungsanordnung eines Kontaktes für eine Anschlussdose |
| JP5557377B2 (ja) * | 2010-03-23 | 2014-07-23 | 矢崎総業株式会社 | 端子の電線に対する接続構造 |
| JP6766735B2 (ja) * | 2017-04-05 | 2020-10-14 | 株式会社オートネットワーク技術研究所 | 内導体端子及びシールドコネクタ |
Family Cites Families (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4168875A (en) * | 1978-06-28 | 1979-09-25 | General Motors Corporation | Electrical connector with welding fixture-connector body |
| DE3234059C2 (de) * | 1982-09-14 | 1986-04-10 | Siemens AG, 1000 Berlin und 8000 München | Lötverbindung |
| US4682840A (en) * | 1983-09-26 | 1987-07-28 | Amp Incorporated | Electrical connection and method of making same |
| AT387108B (de) * | 1986-12-18 | 1988-12-12 | Elektrovac Fabrikation Elektro | Verfahren zur herstellung eines einen isolationskoerperaufweisenden schalterbauteiles |
| DE3708375C1 (en) * | 1987-03-14 | 1988-06-16 | Kostal Leopold Gmbh & Co Kg | Method for connecting a steel cable to an electrical plug contact part |
| JPH01202386A (ja) * | 1988-02-05 | 1989-08-15 | Nippon Koneshisu Kk | 端子のレーザー加工方法およびレーザー加工可能な端子 |
| US4790775A (en) * | 1988-02-09 | 1988-12-13 | E. I. Du Pont De Nemours And Company | Transition connector |
| DE3921990A1 (de) * | 1988-07-08 | 1990-01-11 | Yazaki Corp | Quetschanschlussverbinder fuer leiter und verfahren zur herstellung eines quetschverbinderanschlusses |
| JPH0817108B2 (ja) * | 1989-10-06 | 1996-02-21 | 株式会社東海理化電機製作所 | フラットケーブルとコネクタの接続方法 |
| DE4200492C2 (de) * | 1991-10-04 | 1995-06-29 | Ghassem Dipl Ing Azdasht | Vorrichtung zum elektrischen Verbinden von Kontaktelementen |
| JPH05251124A (ja) * | 1992-03-05 | 1993-09-28 | Mitsubishi Electric Corp | タブ端子 |
| FR2691293A1 (fr) * | 1992-05-15 | 1993-11-19 | Possehl Electronic France Sa | Système de liaison électrique notamment pour circuits hybrides ou autres. |
| JPH06104019A (ja) * | 1992-09-18 | 1994-04-15 | Hitachi Ltd | リードフレームと電線の接続構造 |
| DE9300585U1 (de) * | 1993-01-19 | 1993-05-13 | Holzschuh, Siegfried, 7134 Knittlingen | Stift- oder buchsenförmiger Steckerteil einer elektrischen Steckverbindung |
| JPH088028A (ja) * | 1994-06-23 | 1996-01-12 | Yazaki Corp | 電線の接続方法および電線接続用挟持体 |
| JP3419555B2 (ja) * | 1994-07-22 | 2003-06-23 | 矢崎総業株式会社 | ピン型端子およびその製造方法 |
| JP3373966B2 (ja) * | 1995-02-10 | 2003-02-04 | アルプス電気株式会社 | 回転コネクタ |
-
1997
- 1997-06-10 DE DE19724336A patent/DE19724336A1/de active Pending
-
1998
- 1998-05-16 AT AT98930696T patent/ATE209400T1/de not_active IP Right Cessation
- 1998-05-16 BR BR9810425-0A patent/BR9810425A/pt not_active Application Discontinuation
- 1998-05-16 ES ES98930696T patent/ES2168769T3/es not_active Expired - Lifetime
- 1998-05-16 EP EP98930696A patent/EP0988664B1/de not_active Expired - Lifetime
- 1998-05-16 DE DE59802741T patent/DE59802741D1/de not_active Expired - Lifetime
- 1998-05-16 JP JP50138799A patent/JP2002503382A/ja active Pending
- 1998-05-16 WO PCT/EP1998/002901 patent/WO1998057393A1/de not_active Ceased
- 1998-05-16 KR KR1019997011610A patent/KR100635677B1/ko not_active Expired - Fee Related
- 1998-05-16 US US09/445,776 patent/US20020144398A1/en not_active Abandoned
- 1998-06-09 MY MYPI98002568A patent/MY122253A/en unknown
-
2003
- 2003-12-01 US US10/725,775 patent/US7124501B2/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| US7124501B2 (en) | 2006-10-24 |
| DE19724336A1 (de) | 1998-12-17 |
| DE59802741D1 (de) | 2002-02-21 |
| US20040107567A1 (en) | 2004-06-10 |
| US20020144398A1 (en) | 2002-10-10 |
| BR9810425A (pt) | 2000-09-19 |
| KR100635677B1 (ko) | 2006-10-17 |
| ATE209400T1 (de) | 2001-12-15 |
| EP0988664A1 (de) | 2000-03-29 |
| JP2002503382A (ja) | 2002-01-29 |
| MY122253A (en) | 2006-04-29 |
| KR20010013600A (de) | 2001-02-26 |
| WO1998057393A1 (de) | 1998-12-17 |
| ES2168769T3 (es) | 2002-06-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE202009018730U1 (de) | Verbindungsanordnung an Leiterplatten | |
| DE102009042385A9 (de) | Multi Fork Einpresspin | |
| DE102016218788A1 (de) | Leiterplattenverbindung | |
| DE102006009035A1 (de) | Verfahren zur Herstellung einer Metallklemme und durch das Verfahren hergestellte Metallklemme | |
| EP3698438B1 (de) | Vorrichtung zur elektrischen kontaktierung | |
| EP0433625B1 (de) | Kontaktfederbuchse zum steckbaren Verbinden von Kabeladern und Schaltdrähten | |
| DE112011103017B4 (de) | Elektronische Schaltkreiseinheit zur Anordnung an einem Automatikgetriebe eines Fahrzeugs sowie Herstellungsverfahren hierfür | |
| WO1998057393A1 (de) | Elektrische steckverbindung | |
| DE4222685C2 (de) | Steckkontaktelement | |
| EP0537312A1 (de) | Elektrische verbindungsvorrichtung | |
| DE102005012441A1 (de) | Elektrischer Steckverbinder sowie Verfahren zur Herstellung eines elektrischen Steckverbinders | |
| DE112020004849T5 (de) | Zweiteiliger elektrischer leistungskontakt für einen ladestromkreis eines elektrofahrzeugs | |
| EP1154521A1 (de) | Steckverbinder und Verfahren zur Montage eines Steckverbinders | |
| EP4485486A1 (de) | Elektrohydraulischer aktuator und verfahren zu seiner herstellung | |
| DE102019111847A1 (de) | Weiblicher Einpress-Steckverbinder, Verfahren zur Herstellung eines solchen Steckverbinders, Einpress-Steckverbinder-System und Baugruppe mit einem solchen Einpress-Steckverbinder | |
| DE102008031686A1 (de) | Verbesserte Halteschutzbuchse eines Steckverbinders | |
| DE102021126140A1 (de) | Verbindungselement | |
| DE102006020045B4 (de) | Zwischenstecker und Verfahren zur Herstellung eines Zwischensteckers | |
| EP2544308A1 (de) | Adapterelement zum Verbinden eines Kfz-Kabelbaumes mit einem Flachbandkabel | |
| DE102019206486A1 (de) | Zellverbindungselement und Batteriemodul | |
| WO2013010836A2 (de) | Steckermodul, insbesondere für fensterheberantriebe, sowie verfahren zu dessen herstellung | |
| DE102022125029A1 (de) | Hybrides Kontaktelement | |
| DE102022133909A1 (de) | Kontaktbaugruppe für einen elektrischen Steckverbinder | |
| WO2024165543A2 (de) | Kontaktanordnung sowie verfahren zur herstellung einer solchen | |
| DE102022131107A1 (de) | Leiterplattendirektanschluss |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19991124 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT DE ES FR GB IT |
|
| 17Q | First examination report despatched |
Effective date: 20000714 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT DE ES FR GB IT |
|
| REF | Corresponds to: |
Ref document number: 209400 Country of ref document: AT Date of ref document: 20011215 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| REF | Corresponds to: |
Ref document number: 59802741 Country of ref document: DE Date of ref document: 20020221 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20020201 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2168769 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20080529 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20080416 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20080524 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20080522 Year of fee payment: 11 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20090516 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090516 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090516 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20090518 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090518 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090516 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP Owner name: CONTINENTAL AUTOMOTIVE GMBH, DE Effective date: 20111104 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20130603 Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20150130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140602 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20150531 Year of fee payment: 18 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59802741 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161201 |