EP0872422B1 - Vorrichtung zum Herstellen von Beutelpackungen - Google Patents
Vorrichtung zum Herstellen von Beutelpackungen Download PDFInfo
- Publication number
- EP0872422B1 EP0872422B1 EP98100488A EP98100488A EP0872422B1 EP 0872422 B1 EP0872422 B1 EP 0872422B1 EP 98100488 A EP98100488 A EP 98100488A EP 98100488 A EP98100488 A EP 98100488A EP 0872422 B1 EP0872422 B1 EP 0872422B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- bag
- carry
- receiving means
- conveying device
- gear mechanisms
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 230000007246 mechanism Effects 0.000 claims 6
- 230000008878 coupling Effects 0.000 claims 1
- 238000010168 coupling process Methods 0.000 claims 1
- 238000005859 coupling reaction Methods 0.000 claims 1
- 239000005021 flexible packaging material Substances 0.000 claims 1
- 239000000969 carrier Substances 0.000 description 4
- 230000033001 locomotion Effects 0.000 description 3
- 238000004519 manufacturing process Methods 0.000 description 2
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
- 238000004806 packaging method and process Methods 0.000 description 1
- 238000007789 sealing Methods 0.000 description 1
- 238000007493 shaping process Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/42—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation
- B65B43/46—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation using grippers
- B65B43/465—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation using grippers for bags
Definitions
- the invention is based on a device for manufacturing of bag packs according to the preamble of claim 1.
- the bag which is separated from the end part of the hose, between the Driver of a clocked driven conveyor Locking device in axial alignment with the Bag forming device inserted and drawn in. Since the Application of such an intermittent Device is low, it is desirable to have a Bag pack manufacturing device of the above To create genus similar to other known ones Bag pack making machines works continuously.
- the device according to the invention with the characteristic Features of claim 1 has the advantage that the of Bag forming device prepared bag, be it that this be formed continuously or intermittently, and be that the bags are filled during the molding process, fluent and upright from vertical movement Position transferred into a horizontal movement and in Synchronization with the drivers of the conveyor of the Closing device are brought so that again a flowing lowering of the bags between the carriers is guaranteed.
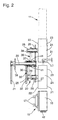
- FIG. 1 shows the end part of a bag forming device, the Input part of a bag closing device and one Bag transfer device in front view and Figure 2 die 1 in side view partially in Cut.
- the pouch pack maker has one Bag-forming device 11 with a vertical shape axis, one Bag closing device 15 with a horizontal conveyor line and a bag transfer device 20 for transferring the from the bag forming device 11 manufactured bag 1 between Driver 16 of a conveyor chain 17 Bag closing device 15.
- the bag forming device 11 is in a manner known per se from a packaging tape a vertical shaped tube 12 or a shaped mandrel a hose 2 shaped, the leading end with a closure seam closed and the end part as a bag 1 from the hose 2 by means of a transverse sealing and cutting device 13 is separated.
- the hose 2 becomes continuous or moved down intermittently.
- the bag 1 can be empty or already when the closure seam is made on End of the hose 2 is filled through the shaped tube 12 receive.
- the transfer device 20 has three gripper-like receptacles 21 with a U-shaped cross section, the two parallel side walls 22, 23 and one of these have connecting rear wall 24.
- the recordings 21 are with a protruding on the side wall 22 pin 25 in one a horizontal axis rotating rotor 27 coaxial rotatably supported, the axes of the bearing eyes 28 plug 25 to the axis of rotation of the rotor 27 on a coaxial circle are evenly distributed.
- the disk-like rotor 27 is in turn on a free one Fixed end of a shaft 29 which in two bearing blocks 31, 32 is rotatably mounted.
- the rotor 27 is like this arranged that the longitudinal axes of the receptacles 21 in one common plane, in which is also the longitudinal axis the bag former 11 and the longitudinal axis of the Conveyor section of the carriers 16 of the transport chain 17 extend. Furthermore, the horizontal axis of the Rotor 27 transverse to the longitudinal axis of the bag-forming device 15 and the conveyor line of the conveyor chain 17 in the corner area between the longitudinal axis of the bag forming device 11 and the part of the conveyor chain 17 running away from this axis.
- the receptacles 21 continuously when the rotor 27 rotates take a position in which they with their longitudinal axis are aligned vertically and their open side against the Axis of the bag forming device 11, they are over Gear connected to a fixed point.
- this gear is a toothed belt gear 35 with one Timing belt 36 wrapped gears 37, 38 formed.
- the common gear 37 serving as a fixed point is seated rotatable on the shaft 29 of the rotor 27 and is with screws 41 rigidly connected to the bearing block 32.
- One gear 38 each the toothed belt gear 35 is one of the free end Pin 25 of the receptacles 21 attached, the gears 38th are staggered so that the looping toothed belt 36 are arranged side by side. It is noted that the vertical alignment of the Recordings 21 other gears during their rotation can be used, such as gear or Dome gear.
- the rotor 27 is via a chain drive 39 or Timing belt drive continuously driven, so that the Recordings 21 tangential to the longitudinal axis of the Move the bag former 11 from top to bottom. there slides one shot 21 after the other with her open side over the moving from top to bottom or advanced hose 2 or via its end part. If the receptacle 21 its the longitudinal axis of the Bag shaping device 11 reaches the nearest position has, the end part of the hose as bag 1 from Hose 2 separated. The bag 1 is then in the receptacle 21 held and carried by means of controlled vacuum.
- the bag 1 receives the arcuate path to the conveyor chain 17 a component of motion that corresponds to the conveying direction of the Conveyor chain 17 is parallel and in the lowest point of the Orbiting the recording 21 a horizontal speed, the is equal to the conveying speed of the conveyor chain 17.
- the vacuum is then switched off and possibly from a nozzle 43 a blast of air from above into the open end of the bag 1 briefly passed so that the Bag 1 between the aligned under the receptacle 21 and carriers moving at the same speed 16 of the conveyor chain 17 falls or is shot where it rests with its bottom on a bottom rail 42 and is taken away.
- the bag 1 If the bag 1 is still in the bag forming device 11 have not received any filling, they will be in the carriers 16 of the conveyor chain 17 first by a filling device and then passed through the bag closing device 15 where the head closure is produced in a known manner. It is also pointed out that in the Bag closing device 15 also a device for Evacuation of the bag 1 can be integrated.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Supplying Of Containers To The Packaging Station (AREA)
- Making Paper Articles (AREA)
Description
Claims (5)
- Vorrichtung zum Herstellen von Beutelpackungen mit einer Beutelformeinrichtung (11) zum Herstellen jeweils eines Beutels (1) von einem vertikal zugeführten Packstoffschlauch, mit einer Beutelschließeinrichtung (15) zum Verschließen von gefüllten Beuteln (1), die eine unterhalb der Beutelformeinrichtung (11) horizontal verlaufende Fördereinrichtung (17) mit Mitnehmern (16) aufweist und mit einer Übergabeeinrichtung (20), welche die von der Beutelformeinrichtung (11) hergestellten Beutel (1) nacheinander in die Mitnehmer (16) der Fördereinrichtung (17) überführt, dadurch gekennzeichnet, daß mehrere im Querschnitt U-förmige Aufnahmen (21) mit je zwei Seitenwände (22, 23) und eine diese verbindende Rückwand (24) an einem um eine horizontale, quer zur Ausrichtung der Beutelformeinrichtung (11) und der Beutelschließeinrichtung (15) gerichtete Achse umlaufenden Rotor (27) auf einem Kreis gleichmäßig verteilt drehbar gelagert und mittels Getrieben mit ihrer Längsachse dauernd senkrecht ausgerichtet sind, so daß sie sich mit ihrer offenen Seite über das Endteil des Schlauches (2) schieben und diesen bei Gleichlauf mit dem Schlauchendteil, wenn dieser vom Schlauch (2) als Beutel (1) abgetrennt wird, fassen und in einem Bogen über die Mitnehmer (16) der kontinuierlich laufenden Fördereinrichtung (17) überführen, und dann den Beutel (1) bei Gleichlauf und Ausrichtung mit einem Mitnehmer (16) der Fördereinrichtung (17) freigeben, so daß dieser in die Mitnehmer (16) der Fördereinrichtung (17) nach unten gleitet.
- Vorrichtung nach Anspruch 1, dadurch gekennzeichnet, daß die die Aufnahmen (21) senkrecht ausrichtenden Getriebe aus je einem Riemengetriebe (35) bestehen, bei dem ein Riemen (36) um ein erstes mit der Aufnahme (21) starr verbundenes Umlenkrad (38) und um ein zweites gleichachsig zur Drehachse des Rotors (27) starr angeordnetes Umlenkrad (37) geschlungen ist.
- Vorrichtung nach Anspruch 1, dadurch gekennzeichnet, daß die die Aufnahmen (21) senkrecht ausrichtenden Getriebe Zahnrad- oder Kuppelgetriebe sind.
- Vorrichtung nach einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, daß die Aufnahmen (21) eine Saugeinrichtung aufweisen, mit der durch Steuern von Unterdruck das Greifen und Loslassen eines Beutels (1) unterstützt wird.
- Vorrichtung nach einem der Ansprüche 1 bis 4, dadurch gekennzeichnet, daß zum Übergeben eines Beutels 1 aus einer Aufnahme (21) in einen Mitnehmer (16) der Fördereinrichtung (17) der Beutelschließeinrichtung (15) an der Übergabestelle eine Blasluftdüse (43) angeordnet ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19715766A DE19715766A1 (de) | 1997-04-16 | 1997-04-16 | Vorrichtung zum Herstellen von Beutelpackungen |
| DE19715766 | 1997-04-16 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0872422A1 EP0872422A1 (de) | 1998-10-21 |
| EP0872422B1 true EP0872422B1 (de) | 2001-05-16 |
Family
ID=7826609
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98100488A Expired - Lifetime EP0872422B1 (de) | 1997-04-16 | 1998-01-14 | Vorrichtung zum Herstellen von Beutelpackungen |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0872422B1 (de) |
| DE (2) | DE19715766A1 (de) |
| ES (1) | ES2157611T3 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117585252B (zh) * | 2024-01-19 | 2024-04-26 | 朗锐包装技术(沧州)有限公司 | 一种三方向运动的取袋机构 |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2937012B2 (ja) * | 1994-04-08 | 1999-08-23 | 時久 増田 | 角筒包装袋の製造方法及び装置 |
| IT1285579B1 (it) * | 1996-03-01 | 1998-06-18 | Gd Spa | Unita' di uscita per una macchina incartatrice continua |
-
1997
- 1997-04-16 DE DE19715766A patent/DE19715766A1/de not_active Withdrawn
-
1998
- 1998-01-14 DE DE59800709T patent/DE59800709D1/de not_active Expired - Lifetime
- 1998-01-14 EP EP98100488A patent/EP0872422B1/de not_active Expired - Lifetime
- 1998-01-14 ES ES98100488T patent/ES2157611T3/es not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| DE19715766A1 (de) | 1998-10-22 |
| EP0872422A1 (de) | 1998-10-21 |
| DE59800709D1 (de) | 2001-06-21 |
| ES2157611T3 (es) | 2001-08-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3141431C2 (de) | Vorrichtung zum Herstellen, Füllen und Verschließen von Beuteln | |
| DE3905605C2 (de) | Verfahren und Vorrichtung zum Herstellen, Füllen und Verschließen von Beuteln | |
| DE2415228C2 (de) | Vorrichtung zum Herstellen und Füllen von Säcken aus thermisch verschweißbarem Material | |
| EP2572996B1 (de) | Verfahren und Vorrichtung zur Herstellung von Beuteln | |
| DE2404826B2 (de) | Vorrichtung zur Formung prismatischer Verpackungsbehälter | |
| DE602006000831T2 (de) | Verfahren und Vorrichtung zum Herstellen eines Beutels mit Ausgusstüllen | |
| DE2629065B2 (de) | Vorrichtung zum automatischen Füllen und Verschließen von Säcken | |
| EP0134754B1 (de) | Verfahren und Vorrichtung zum Antrieb der Siegelelemente einer Verpackungsmaschine | |
| DE4105158A1 (de) | Einrichtung zum warmpressschweissen von verpackungsmaterial in vorrichtungen zum herstellen, fuellen und verschliessen von beuteln | |
| DE19630420B4 (de) | Verfahren zum Betreiben einer Schlauchbeutelmaschine | |
| DE69105063T2 (de) | Automatische Maschine zum Befüllen von Säcken. | |
| EP0345262B1 (de) | Vorrichtung zum herstellen von beuteln | |
| EP0340315A1 (de) | Verfahren und Vorrichtung zur Führung von Säcken an einer Füllstation | |
| EP3459865A1 (de) | Verfahren und vorrichtung zum stapelförmigen verpacken von kleinstückigen produkten | |
| EP0872422A1 (de) | Vorrichtung zum Herstellen von Beutelpackungen | |
| DE68904758T2 (de) | Horizontal arbeitender beutelverpackungsautomat. | |
| DE19808789B4 (de) | Schlauchbeutelmaschine | |
| DE1586328A1 (de) | Verfahren zum Entlasten der Querschweissnaht | |
| EP0057768B1 (de) | Vorrichtung zum Herstellen von Schlauchbeutelpackungen | |
| EP0768242A1 (de) | Verschliessvorrichtung für offene, gefüllte Beutel | |
| DE2519775A1 (de) | Vorrichtung zum wegfuehren von beutelpackungen von einer beutelform-, -fuell- und -schliessmaschine | |
| DE2901053A1 (de) | Maschine zum herstellen, fuellen und verschliessen von beuteln | |
| AT201001B (de) | Maschine zum Füllen von oben offenen Säcken | |
| CH415423A (de) | Verfahren und Vorrichtung zur Herstellung und zum Verschliessen von Beutelpackungen aus schlauchförmigem Material | |
| DE2401193A1 (de) | Vorrichtung zum geordneten einbringen von schlauchbeuteln |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): CH DE ES GB IT LI |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 19990421 |
|
| AKX | Designation fees paid |
Free format text: CH DE ES GB IT LI |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 20000330 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE ES GB IT LI |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: SCINTILLA AG, DIREKTION Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 59800709 Country of ref document: DE Date of ref document: 20010621 |
|
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2157611 Country of ref document: ES Kind code of ref document: T3 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20010731 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20011224 Year of fee payment: 5 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20020124 Year of fee payment: 5 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030114 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030115 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20030115 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20060124 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070131 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070131 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20070504 Year of fee payment: 10 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080114 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20170329 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 59800709 Country of ref document: DE |