EP0640697B1 - Réservoir d'eau et procédé pour sa fabrication - Google Patents
Réservoir d'eau et procédé pour sa fabrication Download PDFInfo
- Publication number
- EP0640697B1 EP0640697B1 EP94108272A EP94108272A EP0640697B1 EP 0640697 B1 EP0640697 B1 EP 0640697B1 EP 94108272 A EP94108272 A EP 94108272A EP 94108272 A EP94108272 A EP 94108272A EP 0640697 B1 EP0640697 B1 EP 0640697B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- chloride
- welding
- wetted
- sulphate
- storage vessel
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images
Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F24—HEATING; RANGES; VENTILATING
- F24H—FLUID HEATERS, e.g. WATER OR AIR HEATERS, HAVING HEAT-GENERATING MEANS, e.g. HEAT PUMPS, IN GENERAL
- F24H1/00—Water heaters, e.g. boilers, continuous-flow heaters or water-storage heaters
- F24H1/18—Water-storage heaters
- F24H1/181—Construction of the tank
- F24H1/183—Inner linings
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23D—ENAMELLING OF, OR APPLYING A VITREOUS LAYER TO, METALS
- C23D3/00—Chemical treatment of the metal surfaces prior to coating
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23D—ENAMELLING OF, OR APPLYING A VITREOUS LAYER TO, METALS
- C23D5/00—Coating with enamels or vitreous layers
- C23D5/02—Coating with enamels or vitreous layers by wet methods
Definitions
- the present invention relates to an internally enamelled steel water tank and to a method for its production according to the preambles of the independent claims.
- the first step was to apply a second layer of enamel, in which the enamelling process was repeated after the first layer of enamel had been fired.
- the need for protective current is then considerably lower, but the production costs of a storage device are greatly increased.
- the present invention has for its object to reduce the defectiveness of the internal enamelling of such a storage container without significantly increasing its manufacturing costs.
- the significantly low protective current requirement is significant for the quality of the enamel obtained compared to the prior art, with hardly increased manufacturing costs.
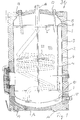
- a hot water tank 31 has a storage housing 1, which is provided on its inside with insulation 2, within which the actual storage tank 3 is mounted.
- the storage container consists of a hollow cylindrical jacket part 4, the upper end 5 and the lower end 6 of which are covered by a base 7 and a cover 8, respectively.
- Bottom and lid are hemispherical structures and exist as well as the jacket part 4 made of unalloyed steel.
- the end 9 of the cover 8 and the end 10 of the bottom 7 are welded to the ends 5 and 6 of the jacket 4.
- the weld seam 18 forms a ring.
- the jacket sheet also has a longitudinal weld 11. All these three weld seams 18 and 11 are located in the interior 32 of the container 3 and are no longer accessible after the entire container 3 has been welded together.
- connecting pieces 14 and 15 can be provided for the passage of a heating element 33 into the interior 32 of the storage container 3, whereby either a water-filled pipe coil or an electric heating element is connected through these connecting pieces. Both alternatives serve for the external heating of the content of the water reservoir 3.
- feet 17 are provided for placing the storage container on a floor.
- recesses can be present, for example in the case of a store which is heated directly by a gas burner, for carrying out the immersion combustion chamber, for providing a cleaning opening, for inserting an anode, a temperature sensor and the like.
- These recesses or pipe sockets are omitted for the sake of simplicity.
- the storage container is manufactured as follows:
- the jacket part 4 is made from a sheet metal strip cut to size, possibly after making any recesses, by bending to the jacket shape, and then the longitudinal weld 11 is welded.
- the lid and base are deep drawn from sheet metal, the holes for any sockets are made, the sockets are welded in if necessary. Then coat and base or lid are degreased, and after degreasing they are freed of adhering layers and contaminants. Then they are roughened by blasting with metal grains.
- an aqueous solution of 50 to 300 g of an alkali or alkaline earth metal sulfate or chloride for example magnesium sulfate (MgSO 4 ), Magnesium chloride (MgCl 2 ), sodium sulfate (Na 2 SO 4 ) or sodium chloride (NaCl) per liter of water or a slurry of zinc sulfide (ZnS), nickel oxide (NiO) or cobalt oxide (Co 3 O 4 ).
- a concentration of 87 g of MgSO 4 per liter of water has proven to be particularly expedient.
- the height of the wetted seam area is also important. It has been found that wetting only a few millimeters on both sides of the weld seam to be provided and wetting of an area of more than 4 cm on both sides of the seam area do not lead to so good results. If an area of 2.0 to 3 cm on both sides of each seam is wetted with this aqueous solution or aqueous slurry, this has an influence on the adhesive behavior of the enamel slip to be applied subsequently, which adheres particularly well in this area. The burning of the angry Email slip then happens as in the prior art.
- the problem of the adhesion of the enamel layer also arises only in the case of weld seams or weld seam sides in the area of the interior 32, that is to say in the area of the reservoir which will no longer be accessible later. External weld spots can be easily cleaned by blasting again with other particles after welding. Accordingly, the two weld seams between cover and middle part and bottom and middle part in the inner region of the storage container 3 are particularly at risk. These areas are therefore wetted.
- the area of the longitudinal weld seam 11 can also be cleaned of welding residues from the inner area by re-treatment by blasting with metal bodies.
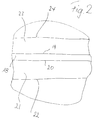
- FIG. 2 shows an enlarged part of the inside view of a weld seam, this weld seam 18 consisting of the actual weld seam area, delimited by the boundary line 19 and 20, the wetted layer on both sides of the weld seam 18 is designated by 21 and 23, its limits by 22 and 24. If you open a store treated in this way, you can see the boundary lines 22 and 23 through elevations on the inside.
- alkali or alkaline earth metal sulfate or chloride preferably MgSO 4
- Wetting with alkali or alkaline earth metal sulfate or chloride, preferably MgSO 4 has the additional advantage of no dangers during handling and storage for the personnel, it is also safe for the user of the storage under food law (DIN safety data sheet 52900). Disposal is also easy.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Combustion & Propulsion (AREA)
- Thermal Sciences (AREA)
- General Engineering & Computer Science (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Physics & Mathematics (AREA)
- Rigid Containers With Two Or More Constituent Elements (AREA)
- Chemical Treatment Of Metals (AREA)
Claims (6)
- Réservoir d'un chauffe-eau à accumulation, émaillé intérieurement et qui comprend un corps à peu près cylindrique et un fond de forme adéquate ainsi qu'un couvercle, tous assemblés par soudure, caractérisé par le fait qu'avant la soudure, les zones de contact respectives sont mouillées d'un sulfate ou d'un chlorure alcalin ou alcalino-terreux, de préférence sulfate ou chlorure de sodium ou de magnésium.
- Réservoir d'un chauffe-eau à accumulation, émaillé intérieurement et qui comprend un corps à peu près cylindrique et un fond de forme adéquate ainsi qu'un couvercle, tous assemblés par soudure, caractérisé par le fait qu'avant la soudure, les zones de contact respectives sont mouillées de sulfure de zinc, oxyde de nickel ou oxyde de cobalt.
- Procédé pour la fabrication d'un réservoir de chauffe-eau à accumulation, émaillé intérieurement et qui comprend un corps à peu près cylindrique et un fond de forme adéquate ainsi qu'un couvercle, composants qui sont d'abord dégraissés et au besoin grenaillés, puis assemblés par soudure et ensuite enduits de bouillie d'émail qui est par la suite soumise à une cuisson, procédé caractérisé par le fait qu'avant la soudure, les zones de contact respectives sont mouillées d'une solution acqueuse d'un sulfate ou d'un chlorure alcalin ou alcalino-terreux, de préférence sulfate ou chlorure de sodium ou de magnésium, ou d'une solution acqueuse de sulfure de zinc, oxyde de nickel ou oxyde de cobalt.
- Procédé suivant la revendication 3, caractérisé par le fait que la concentration de la solution acqueuse se situe entre 50 et 300 g de sulfate de magnésium par litre d'eau.
- Procédé suivant la revendication 3, caractérisé par le fait que la marge de part et d'autre de la soudure a une largeur de 1 à 4 cm, de préférence de 2 à 3 cm .
- Procédé suivant l'une des revendications 3 à 5, caractérisé par le fait que le mouillage est fait sur la face intérieure du réservoir.
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE4319113A DE4319113C1 (de) | 1993-06-05 | 1993-06-05 | Innenemaillierter Wasserbehälter und Verfahren zu seiner Herstellung |
| DE4319113 | 1993-06-05 | ||
| DE4415587 | 1994-04-28 | ||
| DE4415587 | 1994-04-28 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0640697A1 EP0640697A1 (fr) | 1995-03-01 |
| EP0640697B1 true EP0640697B1 (fr) | 1997-08-13 |
Family
ID=25926621
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP94108272A Expired - Lifetime EP0640697B1 (fr) | 1993-06-05 | 1994-05-28 | Réservoir d'eau et procédé pour sa fabrication |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0640697B1 (fr) |
| AT (1) | ATE156869T1 (fr) |
| DE (1) | DE59403711D1 (fr) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6161272A (en) * | 1999-08-23 | 2000-12-19 | Madison; Charles D. | Liquid storage tank apparatus and method of forming same |
| EP3054235A1 (fr) * | 2015-02-09 | 2016-08-10 | Ariston Thermo S.p.A. | Procédé de revêtement pour réservoirs métalliques avec échangeur de chaleur à bobine |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3101274A1 (de) * | 1981-01-16 | 1982-09-02 | Rekord Heizungs- u. Klimageräte Ruckelshausen GmbH u. Co KG, 6102 Pfungstadt | Emaillierverfahren fuer geschlossene behaelter |
-
1994
- 1994-05-28 DE DE59403711T patent/DE59403711D1/de not_active Expired - Lifetime
- 1994-05-28 AT AT94108272T patent/ATE156869T1/de active
- 1994-05-28 EP EP94108272A patent/EP0640697B1/fr not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| DE59403711D1 (de) | 1997-09-18 |
| ATE156869T1 (de) | 1997-08-15 |
| EP0640697A1 (fr) | 1995-03-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3922264C2 (de) | Aus Metall hergestellter Trägerkörper für einen Abgasreinigungskatalysator und Verfahren zu seiner Herstellung | |
| CH638447A5 (de) | Nahtloser behaelter aus metall. | |
| DE3519438A1 (de) | Korrosionsschutzverfahren fuer ein rohr eines dampferzeugers und vorrichtung zur durchfuehrung dieses verfahrens | |
| DE19515425C2 (de) | Innen emaillierter Speicherbehälter für einen Wasserspeicher und Verfahren zu dessen Herstellung | |
| DE4319113C1 (de) | Innenemaillierter Wasserbehälter und Verfahren zu seiner Herstellung | |
| DE7024507U (de) | Doppelwandiges von einer huelle umgebenes rohr | |
| DE3237817A1 (de) | Verfahren zum verbinden von metallteilen durch explosionsschweissen | |
| DE69402646T2 (de) | Verfahren und Vorrichtung zum Herstellen von Flüssiggasflaschen, und hergestellte Flaschen | |
| DE3030595A1 (de) | Verfahren zur herstellung von innen und aussen mit kunststoff beschichteten korrosionsgeschuetzten mehrlagenrohren | |
| EP0640697A1 (fr) | Réservoir d'eau et procédé pour sa fabrication | |
| DE3315544A1 (de) | Heisswasserbereitungsgeraet | |
| DE3048180C2 (de) | Verfahren zum Versehen eines Metallgegenstandes mit einer Schutzschicht | |
| AT262730B (de) | Verfahren zur Herstellung von Flaschen für unter dem Druck eines Treibgases stehende Füllungen | |
| DE102018005065B4 (de) | Dekorationsgegenstand mit edelrost-beschichtung | |
| DE3408206C2 (fr) | ||
| DE3535752C2 (fr) | ||
| DE3123079C2 (fr) | ||
| DE518709C (de) | Mehrwandiges Metallrohr, insbesondere aus mit zugfesten (Eisen-) Schichten abwechselnden korrosionsfesten Schichten | |
| AT129047B (de) | Batteriebecher für elektrische Trockenbatterien. | |
| DE3112154A1 (de) | "behandlungsbehaelter mit als waermetauscher ausgebildetem behaeltermantel" | |
| DE102019105988A1 (de) | Energiespeicherzelle, Energiespeicher sowie Verfahren zum Herstellen einer Energiespeicherzelle | |
| EP0841460A1 (fr) | Caisson pour volet roulant | |
| DE2558575B2 (de) | Thermoelement und verfahren zum herstellen | |
| DE2109628B2 (de) | Brauchwasserbereiter | |
| DE2236069B2 (de) | Geschweißter Behälter mit innerem Rostschutzüberzug |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FR GB GR IE IT LI LU NL PT SE |
|
| 17P | Request for examination filed |
Effective date: 19950720 |
|
| K1C3 | Correction of patent application (complete document) published |
Effective date: 19950301 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 19960722 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: VAILLANT GMBH Owner name: VAILLANT B.V. Owner name: VAILLANT LTD. Owner name: VAILLANT GES.M.B.H Owner name: VAILLANT S.A.R.L Owner name: N.V. VAILLANT S.A. Owner name: JOH. VAILLANT GMBH U. CO. |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FR GB GR IE IT LI LU NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19970813 Ref country code: ES Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19970813 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19970813 |
|
| REF | Corresponds to: |
Ref document number: 156869 Country of ref document: AT Date of ref document: 19970815 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 59403711 Country of ref document: DE Date of ref document: 19970918 |
|
| ITF | It: translation for a ep patent filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19971113 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Effective date: 19971118 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19971110 |
|
| ET | Fr: translation filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980528 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980605 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D Ref document number: 75813 Country of ref document: IE |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20050509 Year of fee payment: 12 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060531 |
|
| BERE | Be: lapsed |
Owner name: *VAILLANT G.M.B.H. Effective date: 20060531 Owner name: *VAILLANT B.V. Effective date: 20060531 Owner name: *VAILLANT LTD Effective date: 20060531 Owner name: *VAILLANT G.M.B.H Effective date: 20060531 Owner name: *VAILLANT S.A.R.L Effective date: 20060531 Owner name: S.A. *VAILLANT N.V. Effective date: 20060531 Owner name: JOH. *VAILLANT G.M.B.H. U. CO. Effective date: 20060531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100528 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20120412 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20130513 Year of fee payment: 20 Ref country code: DE Payment date: 20130509 Year of fee payment: 20 Ref country code: GB Payment date: 20130429 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20130605 Year of fee payment: 20 Ref country code: NL Payment date: 20130507 Year of fee payment: 20 Ref country code: IT Payment date: 20130524 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 59403711 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V4 Effective date: 20140528 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20140527 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK07 Ref document number: 156869 Country of ref document: AT Kind code of ref document: T Effective date: 20140528 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20140527 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20140529 |