EP0346580B1 - Procédé et dispositif pour fabriquer des articles métallisés filiformes - Google Patents
Procédé et dispositif pour fabriquer des articles métallisés filiformes Download PDFInfo
- Publication number
- EP0346580B1 EP0346580B1 EP89106321A EP89106321A EP0346580B1 EP 0346580 B1 EP0346580 B1 EP 0346580B1 EP 89106321 A EP89106321 A EP 89106321A EP 89106321 A EP89106321 A EP 89106321A EP 0346580 B1 EP0346580 B1 EP 0346580B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- chambers
- wire
- drum
- wire shapes
- line
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 35
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 10
- 239000007788 liquid Substances 0.000 claims description 5
- 239000011810 insulating material Substances 0.000 claims description 3
- 239000012777 electrically insulating material Substances 0.000 claims description 2
- 238000005246 galvanizing Methods 0.000 claims description 2
- 238000000926 separation method Methods 0.000 claims description 2
- 238000005259 measurement Methods 0.000 claims 1
- 230000002093 peripheral effect Effects 0.000 claims 1
- 238000009713 electroplating Methods 0.000 abstract description 11
- 230000007246 mechanism Effects 0.000 abstract description 6
- 230000015572 biosynthetic process Effects 0.000 abstract description 2
- 230000014759 maintenance of location Effects 0.000 abstract 1
- 238000009417 prefabrication Methods 0.000 abstract 1
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 description 23
- 229910052759 nickel Inorganic materials 0.000 description 11
- 238000001465 metallisation Methods 0.000 description 9
- 238000007747 plating Methods 0.000 description 8
- 238000005452 bending Methods 0.000 description 3
- 238000005520 cutting process Methods 0.000 description 2
- 229910000831 Steel Inorganic materials 0.000 description 1
- 238000009825 accumulation Methods 0.000 description 1
- 238000005234 chemical deposition Methods 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 230000001427 coherent effect Effects 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 238000005553 drilling Methods 0.000 description 1
- 239000002184 metal Substances 0.000 description 1
- 229910052751 metal Inorganic materials 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
Images




Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C18/00—Chemical coating by decomposition of either liquid compounds or solutions of the coating forming compounds, without leaving reaction products of surface material in the coating; Contact plating
- C23C18/16—Chemical coating by decomposition of either liquid compounds or solutions of the coating forming compounds, without leaving reaction products of surface material in the coating; Contact plating by reduction or substitution, e.g. electroless plating
- C23C18/1601—Process or apparatus
- C23C18/1633—Process of electroless plating
- C23C18/1635—Composition of the substrate
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C18/00—Chemical coating by decomposition of either liquid compounds or solutions of the coating forming compounds, without leaving reaction products of surface material in the coating; Contact plating
- C23C18/16—Chemical coating by decomposition of either liquid compounds or solutions of the coating forming compounds, without leaving reaction products of surface material in the coating; Contact plating by reduction or substitution, e.g. electroless plating
- C23C18/1601—Process or apparatus
- C23C18/1619—Apparatus for electroless plating
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D17/00—Constructional parts, or assemblies thereof, of cells for electrolytic coating
- C25D17/06—Suspending or supporting devices for articles to be coated
Definitions
- the invention relates to a method and a device for the production of metallized, in particular electroless or galvanically nickel-plated, bow-shaped and hook-shaped bent wire parts of the type specified in the preamble of claims 1 and 9.
- Bracket-shaped and hook-like wire shaped parts of this type which are intended, for example, as folding brackets for use in letter folder mechanisms, become more compressible and mutually separable in the course of their manufacturing process, with the formation of a continuous conveyor line in nested and mutually touching, in the conveying direction up to the mutual abutment of their cranked bow webs Order strung together.
- the drum nickel plating which is also known, is not suitable for such complicated shaped wire parts because they get caught in one another in the course of the drum movement, so that their subsequent separation is not possible without complicated handling processes.
- the shaped wire parts can bend during the nickel plating process due to mechanical influences and thereby become unusable for their intended purpose.
- the invention has for its object to improve the method and the device of the type specified in such a way that a simplification of the handling processes and a reduction in the space required in the course of the metallization process is made possible.
- the term “metallization” is to be understood primarily to mean the galvanic or electroless chemical deposition of metal coatings on shaped wire parts, and in particular nickel plating.
- the solution according to the invention is based on the idea that, after the cutting and bending process, the wire blank parts are put together to form a conveyor train with an easily separable order and that this order is maintained in the course of the metallization process.
- individual strand sections with a predetermined number of shaped wire parts are continuously cut off or tapped from the conveyor strand and, in the form of the strand section, immersed in packs in at least one bath provided for carrying out the metallization process and moved through the bath.
- the individual strand sections can then be put together again to form a continuous conveyor strand.
- the shaped wire parts within the strand section are advantageously brought into electrical contact with at least one electrode while maintaining their order directly or indirectly via adjacent shaped wire parts.
- the shaped wire parts are displaced and / or tilted to a limited extent during the metallization process while maintaining their order within each strand section and, if necessary, while maintaining electrical contact with the contact electrode.
- the strand sections are captured in the compressed order, preferably in the area of the stirrup webs, by hand or with a handling device when they are separated from the continuous conveyor strand and / or when they are reassembled into the continuous conveyor strand.
- the strand sections are inserted into chambers made of electrically insulating material with walls perforated for the passage of liquid and inside the chambers with at least one guide rail which expediently extends over the length of the strand section and which can also be designed as an electrode Brought in contact.
- a plurality of chambers arranged in spatial association with one another, each receiving one of the strand sections, are immersed together in the bath and moved through the bath.
- the chambers are expediently arranged on the circumference of a drum and moved through the bath while rotating about the drum axis.
- a plurality of drums are arranged in the circumferential direction and in the longitudinal direction on a drum which can be immersed in a metallization bath and rotatable about its axis therein Chambers are provided for receiving a strand section which is separated from the conveyor strand and contains a number of shaped wire parts in the order of the conveyor strand.
- at least one contact electrode is arranged in the chambers in constant contact with the inserted strand sections.
- the inner dimensions or inner contour of the chambers is adapted to the dimensions of the strand section.
- the chamber walls made of an insulating material have openings for the passage of liquid.
- the guide rails or contact electrodes advantageously have the shape of elongated ribs, rails or strips, which preferably lie in the longitudinal direction of the strand section against the web area of the shaped wire parts.
- two or more guide rails or same-pole contact electrodes can also be arranged on opposite side walls in such a way that they bear against the web area of the shaped wire parts.
- a plurality of flat contact electrodes of the same polarity can be arranged on the inside of the chamber walls, against which the wire shaped parts temporarily come to rest when the chamber is moved through the electroplating bath.
- the contact electrodes arranged in the interior of the chamber are connected as the cathode and at least one electrode arranged outside the chambers in the electroplating bath is connected as the anode.
- the strand sections are preferably aligned in the direction of rotation of the drum in the chambers. In principle, however, it is also possible to arrange the strand sections in the chambers in an axis-parallel orientation to the drum.
- Each strand section advantageously comprises between 10 and 20, advantageously between 12 and 16 shaped wire parts. If with a drum diameter of approx. 40 cm and a drum length of approx. 100 cm a total of about 70 chambers on the drum surface, it follows that each drum contains a total of approx. 1000 wire molded parts in easily manageable, ordered strand sections, which can easily be put together again to form a coherent conveyor strand.
- the wire molded part 10 shown in FIG. 1 is designed as a folding bracket for use in a letter folder mechanism.
- the folding bracket 10 has two legs 12 oriented parallel to one another, which are connected to one another at one end by a vertical web 14 and are curved in a hook shape at their free end 16.
- the web 14 has a crank 18, while in the front ends of the legs 12 blind holes 20 are arranged for receiving the end pins, not shown, line-up pins of the file mechanism.
- the folding brackets steel wire is drawn off from a coil, cut to length in a cutting device and brought into the shape shown in FIG. 1 in a bending station. Subsequently, the blind holes 20 are made and the blanks finished in this way are transferred to a belt conveyor to form a conveyor line.
- the legs 12 are aligned with their hook-shaped ends 16 in the conveying direction and are nested with one another with a lateral offset such that they can be compressed up to the mutual abutment of their cranked webs and can be pushed apart in the conveying direction for parting and removing individual strand sections 24 without interlocking .
- the strand sections 24 can be put together again relatively easily to form a continuous conveyor strand. This knowledge is used in the processing steps described below.
- bracket blanks arriving in the conveyor line 22 from the bending and drilling station must be galvanically (or electrolessly electrolessly) nickel-plated before they are fed to an assembly station to complete the folder mechanism.
- strand sections 24 are tapped from the incoming conveyor strand 22 and gripped by hand or with an automatic handling device in the web area of the stirrups and inserted in packages 30 into chambers 30 of an electroplating drum 32 while maintaining order within the strand.
- the chambers 30 are dimensioned such that the brackets can move relative to one another in a loosened order in the strand direction (cf. FIG. 3).
- the strips 34 are inside the chamber 30 which, due to their shape and arrangement, ensure the guidance and order of the stirrup package regardless of the rotational position of the chamber 30.
- the strips 34 In the case of electroless nickel plating, the strips 34 only have a guiding and holding function.
- the guide strips are at the same time designed as contact electrodes so that a plurality of stirrups 10 of the package 24 are in direct electrical contact with them and the remaining stirrups of the package are electrically connected to them indirectly via the contacting stirrups. This can also be achieved in that several electrodes of the same polarity are arranged on the inner surfaces of the chamber walls distributed over the chamber. In the exemplary embodiments shown in FIGS. 3 to 5, two elongated guide strips or electrodes 34 are arranged in the bottom and top area of the chamber 30, the surface of which, in particular, abuts against the web areas 14 of the bracket.
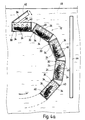
- the chambers are equipped with the stirrup packs 24 via a radially outwardly facing charging opening 36, preferably in the arrangement shown in FIGS. 4a and b, in which the strand sections in the individual chambers are aligned in the direction of rotation of the drum.
- the folding brackets can therefore move against one another in the longitudinal direction, so that undesired shadowing during the galvanizing process is largely avoided.
- the walls 38 of the chambers which are made of insulating material, have openings 40 for the passage of liquid.
- a closing cover 42 on the individual chambers prevents the bracket 10 from rotating the drum 32 can fall out through the loading opening 36.
- a shell which extends over the loading openings and in which the drum 32 is rotatably arranged can also be provided in the lower region of the drum.
- the contact electrodes 34 within the chambers 30 are formed as cathodes during the nickel plating process, while the anode 44 is arranged outside the drum in the electroplating bath. In the area of the anode, there are nickel pellets, not shown, in contact with the anode, which ensure that the nickel which is deposited on the wire molded parts from the nickel bath 46 is continuously fed into the bath.
- the nickel-plated wire molded parts can be removed from the chambers 30 in packages and, while maintaining the strand arrangement, reassembled to form a continuous conveyor strand and can be fed in this form to the subsequent assembly stations.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Electrochemistry (AREA)
- Electroplating Methods And Accessories (AREA)
- Treatment Of Steel In Its Molten State (AREA)
- Wire Processing (AREA)
Claims (22)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT89106321T ATE80419T1 (de) | 1988-06-16 | 1989-04-10 | Verfahren und vorrichtung zum herstellen von metallisierten drahtformteilen. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3820516 | 1988-06-16 | ||
| DE3820516A DE3820516A1 (de) | 1988-06-16 | 1988-06-16 | Verfahren und vorrichtung zum herstellen von metallisierten drahtformteilen |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0346580A1 EP0346580A1 (fr) | 1989-12-20 |
| EP0346580B1 true EP0346580B1 (fr) | 1992-09-09 |
Family
ID=6356684
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89106321A Expired - Lifetime EP0346580B1 (fr) | 1988-06-16 | 1989-04-10 | Procédé et dispositif pour fabriquer des articles métallisés filiformes |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0346580B1 (fr) |
| AT (1) | ATE80419T1 (fr) |
| DE (2) | DE3820516A1 (fr) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19619822C2 (de) * | 1996-05-16 | 1998-04-23 | Elba Buerosysteme Erich Kraut | Aufreihvorrichtung für gelochtes Papiergut o. dgl. und Verfahren zu ihrer Herstellung |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1227036A (fr) * | 1969-02-26 | 1971-03-31 |
-
1988
- 1988-06-16 DE DE3820516A patent/DE3820516A1/de not_active Withdrawn
-
1989
- 1989-04-10 EP EP89106321A patent/EP0346580B1/fr not_active Expired - Lifetime
- 1989-04-10 DE DE8989106321T patent/DE58902236D1/de not_active Expired - Fee Related
- 1989-04-10 AT AT89106321T patent/ATE80419T1/de not_active IP Right Cessation
Also Published As
| Publication number | Publication date |
|---|---|
| DE3820516A1 (de) | 1989-12-21 |
| EP0346580A1 (fr) | 1989-12-20 |
| ATE80419T1 (de) | 1992-09-15 |
| DE58902236D1 (de) | 1992-10-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3703549C2 (de) | Langgestreckte Gestelle und zugehörige Teile zum lösbaren Befestigen von zu galvanisierenden Leiterplatten | |
| CH671526A5 (fr) | ||
| EP0059787B1 (fr) | Appareil pour couvrir d'une couche mince des pièces électroconductrices composées de bandes, de rubans ou analogues pour un procédé éléctrolytrique en continu | |
| DE4108297C2 (de) | Verfahren und Einrichtung zum galvanischen Aufbringen einer metallischen Schicht auf Halbgleitlager | |
| DE2051778A1 (de) | Vorrichtung zum Galvanisieren von zylindrisch geformten Gegenstanden | |
| EP0070011B1 (fr) | Dispositif de galvanisation | |
| WO2000011245A2 (fr) | Dispositif pour le traitement electrochimique partiel d'objets sous forme de barres | |
| DE3638025C2 (de) | Betückungsautomat für axial und radial bedrahtete Bauteile | |
| EP0346580A1 (fr) | Procédé et dispositif pour fabriquer des articles métallisés filiformes | |
| DE2106048A1 (de) | Vorrichtung zum Sammeln diskreter Materialien, insbesondere zur Herstellung von Glasfaserpackungen | |
| EP0150838B1 (fr) | Dispositif de prise de corps creux | |
| DE2740745C2 (de) | Verfahren zur Herstellung von Festelektrolytkondensatoren | |
| DE19803171A1 (de) | Vorrichtung zur Handhabung vorgeformter Einlegeteile und hergestellter Formteile einer Spritzgießmaschine | |
| EP0053676A1 (fr) | Dispositif pour le dépôt électrolytique de l'aluminium | |
| DE1621097A1 (de) | Verfahren und Vorrichtung zur elektrolytischen Herstellung von langgestreckten Metallgegenstaenden,insbesondere von Draehten | |
| DE102016107494A1 (de) | Verfahren und Vorrichtung zum Entnehmen von Batteriezellen aus einer rechteckigen Umverpackung | |
| EP2243394A1 (fr) | Procédé de formation d'un faisceau de poils et dispositif approprié à l'exécution du procédé | |
| DE1172512B (de) | Haltevorrichtung fuer perforierte Tauch-trommeln bei Anlagen zur Oberflaechen-behandlung von Massenteilen in Fluessigkeiten | |
| DE10108332A1 (de) | Drahtzuführung | |
| EP0522232A2 (fr) | Electrode pour l'enlèvement de métaux de solutions contenant des ions métalliques | |
| DE69408312T2 (de) | Aufnahmebehälter für elektronische Teile | |
| DE3114633C2 (fr) | ||
| DE4007984C1 (fr) | ||
| EP1003626A1 (fr) | Procede et dispositif pour la fabrication de broches, notamment de broches de pile | |
| DE7818903U1 (de) | Schlenkerkathode fuer einen elektrochemischen apparat |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19891006 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT CH DE FR GB IT LI NL |
|
| 17Q | First examination report despatched |
Effective date: 19910923 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT CH DE FR GB IT LI NL |
|
| REF | Corresponds to: |
Ref document number: 80419 Country of ref document: AT Date of ref document: 19920915 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 58902236 Country of ref document: DE Date of ref document: 19921015 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| ET | Fr: translation filed | ||
| ITF | It: translation for a ep patent filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19930310 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 19930311 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19930315 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19930316 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19930427 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19930430 Year of fee payment: 5 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19940410 Ref country code: AT Effective date: 19940410 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19940430 Ref country code: CH Effective date: 19940430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19941101 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19940410 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19941229 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19950103 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050410 |