EP4069593B1 - Horizontalformvorrichtung - Google Patents
Horizontalformvorrichtung Download PDFInfo
- Publication number
- EP4069593B1 EP4069593B1 EP20816976.3A EP20816976A EP4069593B1 EP 4069593 B1 EP4069593 B1 EP 4069593B1 EP 20816976 A EP20816976 A EP 20816976A EP 4069593 B1 EP4069593 B1 EP 4069593B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- unit
- packaging material
- mold
- forming
- horizontal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H18/00—Winding webs
- B65H18/08—Web-winding mechanisms
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B51/00—Devices for, or methods of, sealing or securing package folds or closures; Devices for gathering or twisting wrappers, or necks of bags
- B65B51/10—Applying or generating heat or pressure or combinations thereof
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
- B65B9/06—Enclosing successive articles, or quantities of material, in a longitudinally-folded web, or in a web folded into a tube about the articles or quantities of material placed upon it
- B65B2009/063—Forming shoulders
Definitions
- the invention is based on a horizontal forming device, in particular for horizontal tubular bag machines, with at least one, in particular roll-free, forming unit, in particular a forming shoulder, which is intended to form a packaging material web, in particular a paper web, into a packaging material tube, the forming unit having at least one folding edge has, around which the packaging material web can be deflected, and with at least one mold guide unit, in particular a further mold shoulder, which is intended to hold the packaging material tube transversely to an inlet direction of the packaging material web on the molding unit while maintaining a to continue the material tension generated by the molding unit, in particular homogeneous.
- the horizontal molding device comprises at least one support surface, in particular a worktop, on which products to be packaged can be transported, the molding unit and the mold guide unit being arranged on sides of the support surface facing away from one another, the mold guide unit comprising at least one mold guide contour which is used for this purpose It is intended to support the guided packaging material tube in order to maintain the homogeneous material tension.
- a packaging machine in particular a horizontal tubular bag machine, comprises the horizontal forming device.
- the horizontal shaping device is intended to guide a packaging material, in particular the packaging material tube, along a horizontal transport direction, in particular along a transport direction that runs at least substantially perpendicular to a gravitational force direction.
- substantially perpendicular is intended to define in particular an orientation of a direction relative to a reference direction, wherein the direction and the reference direction, in particular viewed in a projection plane, enclose an angle of 90° and the angle has a maximum deviation of in particular less than 8° , advantageously smaller than 5° and particularly advantageously smaller than 2°.
- Provided is intended to mean, in particular, specially programmed, specially designed and/or specially equipped.
- the fact that an object is intended for a specific function should be understood in particular to mean that the object fulfills and/or executes this specific function in at least one application and/or operating state.
- the horizontal shaping device is provided at least for shaping and/or guiding a web of packaging material, the packaging material preferably being designed as a paper.
- the packaging material web is designed as a paper web.
- the horizontal shaping device can be provided in addition to or at least as an alternative to shaping and/or guiding a web of packaging material, the packaging material being designed differently from paper, for example as a plastic.
- the packaging material web can alternatively be made of a plastic.
- the packaging material is in particular for packaging, in particular for a wrapping Products, especially food products.
- the packaging material is preferably designed as packaging paper.
- a “packaging material web” should in particular be a flat, in particular two-dimensional, Configuration of the packaging material, in particular the packaging paper, can be understood.
- the packaging machine comprises at least one packaging material unwinding unit, which is intended to receive the packaging material, in particular as a packaging material roll.
- the packaging material unwinding unit is intended to unwind the packaging material as a packaging material web, in particular to feed it to a packaging material supply unit of the packaging machine.
- the packaging material supply unit is intended in particular to supply the packaging material web to the horizontal forming device, in particular to the forming unit.
- the packaging material supply unit can comprise a plurality of components, in particular known to a person skilled in the art, such as at least one rocker arm, at least one centering button, at least one web edge control and/or at least one printing unit for printing on the packaging material.
- a “packaging material tube” is to be understood in particular as meaning a configuration of the packaging material, in particular the packaging paper, which is formed, in particular at least transversely to a web plane of the packaging material web.
- the packaging material tube is intended to wrap products to be packaged.
- the packaging machine has at least one product feed unit, in particular a conveyor belt, a driver chain or the like, which is intended to transport the products to be packaged into a wrapping through the packaging material tube into an area of the horizontal forming device, in particular the forming unit.
- a transport direction of the products runs at least essentially parallel to a transport direction of the packaging material tube.
- substantially parallel is intended to mean, in particular, an alignment of a direction relative to a reference direction, in particular in a plane, with the direction having a deviation from the reference direction, in particular less than 8°, advantageously less than 5° and particularly advantageously less than 2 ° has.
- the product feed unit is arranged in front of the horizontal forming device, in particular in front of the forming unit, along the transport direction of the packaging material tube.
- the packaging machine comprises at least one longitudinal sealing unit, which is intended to create a longitudinal sealing seam of the packaging material tube, in particular at least substantially parallel to the transport direction of the packaging material tube, in particular by heat input into the packaging material and/or by pressure on the packaging material.
- the longitudinal sealing unit is arranged along the transport direction of the packaging material tube after the horizontal forming device, in particular after the mold guiding unit.
- the longitudinal sealing unit comprises at least one pair of sealing rollers, in particular provided with a profile, which can be pressurized and/or heated and which are intended to transport the packaging material tube, in particular by rotation.
- the longitudinal sealing unit preferably comprises a plurality of pairs of sealing rollers, wherein at least a first pair of sealing rollers arranged along the transport direction of the packaging material tube after the horizontal forming device is designed to be heat-free, in particular for heating-free transport of the packaging material tube.
- the packaging machine comprises at least one transverse sealing unit, which is intended to create transverse sealing seams of the packaging material tube, in particular after each product, which in particular run at least substantially perpendicular to the transport direction of the packaging material tube, in particular by targeted pressure on the packaging material and/or through a heat input into the packaging material.
- the transverse sealing unit is intended to separate the packaging material tube into individual packages, each of which in particular encloses a product.
- the transverse sealing unit is arranged along the transport direction of the packaging material tube after the longitudinal sealing unit.
- the molding unit is preferably intended to deflect the web of packaging material.
- the packaging material supply unit is intended to supply the packaging material web to the molding unit along a direction that runs transversely, in particular at least substantially perpendicular, to the transport direction of the packaging material tube.
- the molding unit has at least one folding edge around which the packaging material web is redirectable.
- the folding edge is preferably designed as a shoulder edge and the molding unit is designed as a molding shoulder.
- the molding unit is designed to be free of rollers to deflect the packaging material web.
- the molding unit is intended to deflect the packaging material web at the folded edge in a direction transverse to the inlet direction of the packaging material web and transverse to the transport direction of the packaging material tube.
- the folded edge extends at least substantially perpendicular to the inlet direction of the packaging material web and to the transport direction of the packaging material tube.
- the folded edge is intended to generate a homogeneous material tension in the packaging material.
- the molding unit preferably has at least two mold contour edges which, starting from the folded edge, extend transversely to the folded edge, in particular in a V-shape.
- the packaging material web can be formed around the mold contour edges into the packaging material tube.
- the mold contour edges extend along a running direction of the packaging material and/or along an outer contour of the supplied products from the folding edge to a molding tunnel of the molding unit, which is intended to guide the packaging material tube along the transport direction of the packaging material tube.
- a longitudinal axis of the mold tunnel runs at least substantially parallel to the transport direction of the packaging material tube.
- the mold guide unit is preferably intended to guide the packaging material tube at least essentially perpendicular to the inlet direction of the packaging material web on the molding unit, in particular along the transport direction of the packaging material tube, while maintaining the homogeneous material tension generated by the molding unit, in particular by the folding edge.
- the mold guide unit is arranged along the transport direction of the packaging material tube after the mold unit and in particular in front of the longitudinal sealing unit.
- the shape guide unit comprises at least one, in particular three-dimensional, shape guide contour, which is intended to support the guided packaging material tube, in particular at least one outer edge of the packaging material tube, to achieve maintenance the homogeneous material tension.
- the mold guide unit has at least two mold guide contours, which in particular are mirror-symmetrical about an imaginary plane of symmetry which extends at least substantially parallel to the transport direction of the packaging material tube, in which in particular the transport direction of the packaging material tube runs, and which is at least substantially perpendicular to the folded edge of the Forming unit extends, are arranged.
- the mold guide unit is designed to be mirror-symmetrical, in particular around the imaginary plane of symmetry.
- the mold guide unit and/or the mold unit are/is designed asymmetrically.
- the mold guide unit is designed without rollers to deflect the packaging material tube, in particular as a further mold shoulder.
- the mold guide unit can have a geometry that is at least essentially analogous to a geometry of the mold unit.
- the support surface preferably forms a piece of track on which the products can be transported.
- the support surface preferably extends at least substantially parallel to the transport direction of the packaging material tube.
- the product feed unit, the longitudinal sealing unit, in particular the sealing rollers, and/or the transverse sealing unit are/is arranged at least in sections within the support surface and extend/extend at least in sections through the support surface.
- axes of rotation of the sealing rollers of the longitudinal sealing unit run at least substantially perpendicular to the support surface.
- the molding unit is arranged on a side of the support surface on which the products can be transported and on which in particular the packaging material unwinding unit and the packaging material supply unit are arranged.
- the mold guide unit is preferably arranged on a further side of the support surface, on which in particular the longitudinal sealing unit is arranged at least to a large extent, in particular more than 50% of a maximum extent of the longitudinal sealing unit, at least essentially parallel to the axes of rotation of the sealing rollers.
- the mold guide unit can be coupled to the support surface at least in sections.
- the packaging material tube extends at least in sections through the support surface, in particular onto the further side of the support surface.
- the packaging material tube can advantageously be guided precisely on two sides of the support surface facing away from one another. It can advantageously be possible to precisely form a packaging material web into a packaging material tube.
- Packaging material webs made of sensitive, especially tear-prone and/or very thin materials, especially paper, can advantageously be formed into packaging material tubes. At least essentially wrinkle-free packaging tubes can advantageously be produced.
- An advantageously compact horizontal forming device can be provided.
- the mold guide unit is designed, in particular arranged, separately from the mold unit.
- the mold guide unit is preferably designed as an independent component or as an independent assembly, in particular made up of two symmetrical components.
- the mold guide unit is arranged at a distance from the molding unit along a direction that is at least substantially perpendicular to the transport direction of the packaging material tube, in particular along the inlet direction of the packaging material web, and/or along the transport direction of the packaging material tube.
- the mold guide unit is designed in one piece with the mold unit, in particular as a mold guide extension of the mold unit.
- the term “one-piece” is intended to mean, in particular, formed in one piece.
- this one piece is produced from a single blank, a mass and/or a casting, particularly preferably in an injection molding process, in particular a single and/or multi-component injection molding process. Precise guidance of the packaging material tube over a long distance can advantageously be made possible.
- the horizontal forming device has at least one, in particular U-shaped, product and/or packaging material guide tunnel, which is intended to support the packaging material tube.
- the product and/or packaging material guide tunnel can in particular be on the side of the support surface facing the molding unit arranged, in particular attached to the support surface.
- the product and/or packaging material guide tunnel can extend in particular along the transport direction of the packaging material tube from at least in front of the molding unit to the molding unit, preferably to the molding guide unit and particularly preferably to the first pair of sealing rollers of the longitudinal sealing unit.
- the product and/or packaging material guide tunnel has a cross section that is at least substantially analogous to a cross section of products to be packaged, in particular a slightly larger cross section than the products to be packaged.
- the products can be transported within the product and/or packaging material guide tunnel.
- the molding unit is intended to shape the packaging material tube at least in sections around the product and/or packaging material guide tunnel, in particular around outer edges of the product and/or packaging material guide tunnel.
- the product and/or packaging material guide tunnel is intended to support the packaging material tube, in particular in addition to the mold guide unit.
- the horizontal forming device and the packaging machine are designed to be free of a product and/or packaging material guide tunnel. Precise enclosing of the products can advantageously be made possible.
- the horizontal forming device comprises at least one adjustment unit, which is intended to adjustably mount the forming unit and the forming guide unit in order to realize different packaging material tube geometries, in particular in different adjustment planes.
- the horizontal forming device comprises at least two adjustment units, one adjustment unit being provided to adjustably mount the forming unit, and another adjustment unit being intended to adjustably mount the form guide unit.
- different packaging material tube geometries may be required for packaging different products.
- the packaging machine is intended for packaging different products, which in particular have different dimensions.
- different packaging material tube geometries can be used for packaging different products, which have different maximum Extensions at least substantially perpendicular to the support surface, in particular different heights, and/or which have different maximum extensions at least substantially parallel to the support surface and transverse to the transport direction of the packaging material tube, in particular different widths, are required.
- a maximum extension of the packaging material tube is/is at least essentially perpendicular to the support surface, in particular a height of the packaging material tube, and/or a maximum extension of the packaging material tube is at least substantially parallel to the support surface and transversely to the transport direction of the packaging material tube, in particular a width of the packaging material tube, adjustable.
- the shape guide unit can be adjustable by means of the further adjustment unit to correct uneven tension conditions in the packaging material.
- the molding unit is adjustable in at least one adjustment plane extending on the side of the support surface facing the molding unit.
- the mold guide unit is adjustable in at least one further adjustment plane extending on the further side of the support surface facing the mold guide unit.
- the mold unit and/or the mold guide unit are/are mounted adjustably as a whole component or as a whole assembly.
- the mold unit and/or the mold guide unit are/is adjustable in themselves, in particular individual components of the mold unit relative to one another and/or individual components of the mold guide unit relative to one another.
- a horizontal forming device can be provided which enables an advantageous, format-flexible adaptation of a packaging material tube geometry to different products to be packaged.
- the at least one adjustment unit in particular the adjustment units, is/are intended to mount the mold unit and the mold guide unit so that they can be adjusted relative to one another.
- the adjustment units are intended to make the mold unit and the mold guide unit adjustable relative to one another as a whole component or as a whole assembly to store.
- the adjustment units are intended to mount the mold unit and the mold guide unit in a linearly movable and/or pivoting manner.
- the adjustment unit is provided to support the molding unit, in particular for adjusting a height of the packaging material tube, in an at least linearly movable manner along an adjustment direction that runs at least substantially perpendicular to the support surface.
- the adjustment unit is intended to support the molding unit in a linearly movable manner along a further adjustment direction that runs at least substantially perpendicular to the adjustment direction and at least essentially parallel to the transport direction of the packaging material tube.
- the further adjustment unit is provided to mount the mold guide unit at least in a linearly movable manner along at least one adjustment direction that runs at least substantially parallel to the support surface, in particular transversely to the transport direction of the packaging material tube.
- the setting units are preferably designed as manual setting units for manual adjustment of the mold unit and the mold guide unit, in particular relative to one another.
- At least one of the adjustment units has at least one automatic adjustment element, in particular a servomotor, which is provided for automatic adjustment of the mold unit and/or the mold guide unit.
- at least one of the adjustment units has at least one automatic adjustment element, in particular a servomotor, which is provided for automatic adjustment of the mold unit and/or the mold guide unit.
- the at least one adjustment unit in particular the adjustment units, is/are intended to mount at least two mold legs of the mold unit and/or the mold guide unit so that they can be adjusted relative to one another.
- the mold unit has at least two mold legs which are mounted so that they can be adjusted relative to one another, in particular so that they can be moved linearly and/or pivotally.
- the mold legs of the mold unit are mounted so that they can move at least linearly relative to one another, in particular along a direction that runs at least substantially parallel to the fold edge, in particular to a fold edge running surface.
- the mold legs of the mold unit jointly form the folding edge, in particular the folding edge running surface.
- the mold legs the molding unit in particular along the direction running at least essentially parallel to the fold edge, in particular to the fold edge running surface, is mounted movably towards and away from each other, in particular to adjust a width of the packaging material tube.
- the mold legs of the molding unit together form the molding tunnel of the molding unit.
- each mold leg of the mold unit forms at least one mold contour edge of the mold unit.
- the adjustment unit preferably has at least one intermediate element, in particular a plurality of intermediate elements, to fill a space between the two mold legs of the mold unit that move away from one another, in particular to ensure different product widths.
- the mold guide unit has at least two mold legs which are mounted so that they can be adjusted relative to one another, in particular in a linearly movable and/or pivoting manner.
- the further adjustment unit which is provided for adjustable mounting of the mold guide unit, can be designed at least substantially analogously to the adjustment unit, which is provided for adjustable storage of the mold unit.
- the mold legs of the mold guide unit are mounted so that they can move at least linearly relative to one another.
- the further adjustment unit is intended to mount the mold legs of the mold guide unit in a linearly movable manner along different, in particular transverse, adjustment directions, in particular to ensure different product widths.
- the adjustment directions run in a common plane, in particular extending at least substantially parallel to the support surface, and in particular include equal angles with the transport direction of the packaging material tube.
- the mold legs of the mold guide unit can be mounted so that they can be at least pivotally movable relative to one another, in particular in a pivot plane that extends at least substantially parallel to the support surface, in particular to adjust the width of the packaging material tube.
- the mold legs of the mold guide unit can be pivotally mounted on an end region of the mold limbs of the mold guide unit facing away from the mold unit along the transport direction of the packaging material tube.
- the can End region of the mold legs of the mold guide unit can be formed, in particular mounted, separately from a remaining region of the mold guide unit, in particular separated from the remaining region along a separating cut.
- each mold leg of the mold guide unit forms at least one mold guide contour of the mold guide unit.
- the mold legs of the mold guide unit are arranged, in particular mounted, mirror-symmetrically to one another around the imaginary plane of symmetry.
- a positioning of mold legs of the mold unit and/or the mold guide unit relative to one another that is optimized for different products and/or packaging materials can be made possible.
- the mold legs of the mold guide unit form a V-shaped tapered guide region in the transport direction of the packaging material tube, which is intended to bring together seam regions of the packaging material tube that are to be sealed with one another.
- the guide area is intended to bring together longitudinal sealing seam areas of the packaging material tube that are to be sealed with one another.
- the mold legs of the mold guide unit have a greater distance from one another in an end region facing the mold unit along a direction that runs at least substantially parallel to the support surface and at least substantially perpendicular to the transport direction of the packaging material tube than in the end region facing away from the mold unit.
- the seam areas of the packaging material tube are in particular areas in which the packaging material, in particular the packaging paper, is sealed, in particular to create a sealing seam.
- the guide area is intended to bring the seam areas together in such a way that the seam areas can be transported between two sealing rollers of the pairs of sealing rollers to form a seal.
- the guide area opens in the end area facing away from the molding unit into a support contour formed by the mold legs of the molding guide unit, which is intended to support the packaging material tube, in particular the joined seam regions, in particular during further transport to the longitudinal sealing unit. Precise alignment of the seam areas to achieve a clean sealing seam, in particular a longitudinal sealing seam, can advantageously be made possible.
- the horizontal molding device comprises at least one heating unit, which is intended to heat the molding unit and/or the mold guide unit at least in sections, in particular to introduce heat into one, in particular into the aforementioned, seam area.
- the heating unit is intended to enable heat input into the packaging material, in particular into the packaging paper, prior to a sealing, in particular a longitudinal sealing, of the packaging material, in particular the packaging paper.
- the heating unit is intended to seal the packaging material, in particular the packaging paper, in particular on the mold guide unit, in particular as an alternative to sealing by the longitudinal sealing unit, and/or to ensure an increased heat input, in particular in one area the support contour of the mold guide unit.
- the heating unit can in particular be designed as a heating coil, as a heating cartridge, as a heating plate, as a thick-film heating element or as another heating unit that appears sensible to a person skilled in the art.
- the heating unit is preferably arranged on the mold unit and/or on the mold guide unit, and is in particular in direct contact with the mold unit and/or the mold guide unit.
- the horizontal molding device can have a plurality of heating units, wherein at least one heating unit can be assigned to the molding unit and at least one further heating unit can be assigned to the mold guide unit.
- the heating unit is arranged on a side of the mold unit and/or the mold guide unit facing away from a contact surface with the packaging material, in particular with the packaging paper.
- a heater which is arranged parallel to a surface of the molding unit, in particular at a distance from the molding unit, is conceivable, which heats the packaging material on an inside.
- the molding unit and/or the molding guide unit are intended to transfer thermal energy absorbed by the heating unit to the packaging material, in particular to the packaging paper.
- the mold unit, in particular the mold legs of the mold unit, and/or the mold guide unit, in particular the mold legs of the mold guide unit are made of a thermally conductive material, in particular a metal.
- the molding unit and/or the molding guide unit on the contact surface with the packaging material, in particular with the packaging paper is/are intended to transfer thermal energy provided by the heating unit to the packaging material, in particular in the seam areas.
- at least one sealing layer of the packaging paper can be activated by applying heat to the seam areas. An efficient sealing of the packaging material, in particular the packaging paper, can advantageously be made possible.
- the horizontal molding device comprises at least one air pressure unit, which is intended to exert a negative pressure and/or an excess pressure on a packaging material on the molding unit and/or on the mold guide unit.
- a “negative pressure” is intended to mean, in particular, an air pressure that is lower than an ambient air pressure of the horizontal forming device.
- An “overpressure” is intended to mean, in particular, an air pressure that is higher than an ambient air pressure of the horizontal forming device.
- the air pressure unit can in particular be designed as a blower, as a vacuum cleaner or as another air pressure unit that appears useful to a person skilled in the art.
- the horizontal molding device can have a plurality of air pressure units, wherein at least one air pressure unit can be assigned to the mold unit and at least one further air pressure unit can be assigned to the mold guide unit.
- the air pressure unit is arranged on the side of the mold unit and/or the mold guide unit facing away from the contact surface with the packaging material, in particular with the packaging paper.
- the mold unit, in particular the mold legs of the mold unit, and/or the mold guide unit, in particular the mold legs of the mold guide unit are perforated at least in sections, in particular made of a porous material.
- air from an air flow generated by the air pressure unit can flow at least in sections through the mold unit and/or the mold guide unit.
- the air pressure unit is intended to generate a negative pressure for suction of the packaging paper onto the molding unit and/or onto the molding guide unit, in particular to achieve a low-crease contact of the packaging paper on the molding unit and/or on the molding guide unit.
- the air pressure unit intended to generate an overpressure to form an air cushion on the mold unit and/or on the mold guide unit, in particular to realize low-friction transport of the packaging paper along the mold unit and/or along the mold guide unit.
- the air pressure unit can be switched between generating a negative pressure and generating an excess pressure, in particular depending on an application situation, for example depending on a packaging material used.
- a particularly material-friendly transport of the packaging paper can be made possible.
- the horizontal forming device comprises at least one driven pressure unit, in particular a pressure roller, which is intended to apply a pressure force to a packaging material against the mold guide unit.
- the horizontal molding device comprises the at least one driven pressure unit as an alternative or in addition to an air pressure unit assigned to the mold guide unit.
- the horizontal forming device comprises at least two driven pressure units, with at least one driven pressure unit being assigned to a mold leg of the mold guide unit, in particular being intended to apply a pressure force to the packaging material against the mold leg.
- the horizontal forming device comprises at least one additional driven pressure unit, in particular an additional pressure roller, which is intended to apply a pressure force to the packaging material against the molding unit.
- the driven pressure units are preferably designed as pressure rollers which can be driven to perform rotational movements, in particular to transport the packaging material tube along the transport direction of the packaging material tube.
- the driven pressure units are intended to guide the packaging material tube between the driven pressure units and the mold guide unit, in particular the mold legs of the mold guide unit. Particularly precise guidance of the packaging material can advantageously be made possible.
- the invention is based on a packaging machine, in particular a horizontal tubular bag machine, with at least one horizontal forming device according to the invention.
- the packaging machine additionally comprises at least the packaging material unwinding unit, the packaging material supply unit, the product supply unit, the longitudinal sealing unit and the transverse sealing unit.
- a packaging machine can advantageously be provided that enables products to be packaged in a particularly gentle way on materials.
- the horizontal forming device according to the invention and/or the packaging machine according to the invention should not be limited to the application and embodiment described above.
- the horizontal forming device according to the invention and/or the packaging machine according to the invention can have a number of individual elements, components and units that deviate from the number mentioned herein in order to fulfill a function of operation described herein.
- values lying within the stated limits should also be considered disclosed and can be used in any way.
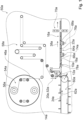
- FIG. 1 shows part of a packaging machine 50a in a schematic representation.
- the packaging machine 50a preferably comprises a horizontal forming device 10a, in particular for horizontal tubular bag machines, with at least one, in particular roll-free, forming unit 12a, in particular a forming shoulder, which is intended to form a packaging material web 14a, in particular a paper web and/or a film web, into a packaging material tube 16a to shape.
- the packaging machine 50a is designed in particular as a horizontal tubular bag machine.
- the horizontal shaping device 10a is intended to guide a packaging material 46a, in particular the packaging material tube 16a, along a horizontal transport direction 38a, in particular along a transport direction 38a that runs at least substantially perpendicular to a gravitational force direction 52a.
- the horizontal shaping device 10a is provided at least for shaping and/or guiding the packaging material web 14a, with the packaging material 46a preferably being designed as a paper and/or as a film.
- the packaging material web 14a is designed as a paper web and/or as a film web.
- the horizontal forming device 10a can be provided in addition to or at least as an alternative to forming and/or guiding a packaging material web 14a, with the packaging material 46a being designed differently from paper, for example as a plastic.
- the packaging material web 14a can alternatively be made of a plastic.
- the packaging material 46a is intended in particular for packaging, in particular for a wrapping, of products 24a, in particular food products (cf. Figure 3 ).
- the packaging material 46a is preferably designed as packaging paper.
- the packaging machine 50a comprises at least one packaging material unwinding unit 54a, which is intended to receive the packaging material 46a, in particular as a packaging material roll 56a.
- the packaging material unwinding unit 54a is intended to unwind the packaging material 46a as a packaging material web 14a, in particular to feed it to a packaging material supply unit 58a of the packaging machine 50a.
- the packaging material supply unit 58a is intended in particular to supply the packaging material web 14a to the horizontal forming device 10a, in particular to the forming unit 12a.
- the packaging material supply unit 58a can comprise a plurality of components, in particular known to a person skilled in the art, such as at least one rocker arm, at least one centering button, at least one web edge control and/or at least one printing unit for printing on the packaging material 46a.
- the packaging material tube 16a is intended to envelop products 24a to be packaged.
- the packaging machine 50a has at least one product feed unit 60a, in particular a conveyor belt, a driver chain or the like, which is intended to wrap the products 24a to be packaged through the packaging material tube 16a into an area of the horizontal molding device 10a, in particular the molding unit 12a, to transport.
- the packaging machine 50a comprises at least one longitudinal sealing unit 64a, which is intended to create a longitudinal sealing seam of the packaging material tube 16a, in particular at least substantially parallel to the transport direction 38a of the packaging material tube 16a, in particular by pressure on the packaging material 46a and/or by a Heat input into the packaging material 46a.
- the longitudinal sealing unit 64a is arranged along the transport direction 38a of the packaging material tube 16a after the horizontal forming device 10a, in particular after a mold guide unit 18a of the horizontal forming device 10a (see FIG. 2).
- the longitudinal sealing unit 64a comprises at least one pair of sealing rollers 66a, 68a, in particular heatable, profiled and/or pressurizable, which are intended to transport the packaging material tube 16a, in particular by rotation (cf. Figure 2 ).
- the longitudinal sealing unit 64a preferably comprises a plurality of pairs of sealing rollers 66a, 68a, with at least a first pair of sealing rollers 66a arranged along the transport direction 38a of the packaging material tube 16a after the horizontal forming device 10a being designed to be heat-free, in particular for heating-free transport of the packaging material tube 16a.
- the packaging machine 50a preferably comprises at least one transverse sealing unit 70a, which is intended, in particular after each product 24a, to create transverse sealing seams of the packaging material tube 16a, which in particular run at least substantially perpendicular to the transport direction 38a of the packaging material tube 16a, in particular by applying pressure the packaging material 46a and/or by heat input into the packaging material 46a.
- the transverse sealing unit 70a is intended to separate the packaging material tube 16a into individual packages, each of which in particular encloses a product 24a.
- the transverse sealing unit 70a is arranged along the transport direction 38a of the packaging material tube 16a after the longitudinal sealing unit 64a.
- the molding unit 12a is preferably intended to deflect the packaging material web 14a.
- the packaging material supply unit 58a is intended to supply the packaging material web to the molding unit 12a 14a along a direction, in particular inlet direction 20a, which runs transversely, in particular at least essentially perpendicularly, to the transport direction 38a of the packaging material tube 16a.
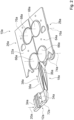
- FIG 2 shows a part of the horizontal forming device 10a of the packaging machine 50a Figure 1 in a schematic perspective view.
- the horizontal forming device 10a preferably comprises at least one, in particular the aforementioned, mold guide unit 18a, in particular a further molding shoulder, which is intended to move the packaging material tube 16a transversely to an, in particular transversely to the aforementioned, inlet direction 20a of the packaging material web 14a on the molding unit 12a while maintaining a to continue the material tension generated by the molding unit 12a, in particular homogeneous.
- the molding unit 12a preferably has at least one folding edge 72a around which the packaging material web 14a can be deflected.
- the folding edge 72a is preferably designed as a shoulder edge and the molding unit 12a as a molding shoulder.
- the molding unit 12a is designed to be free of rollers to deflect the packaging material web 14a.
- the molding unit 12a is intended to deflect the packaging material web 14a at the folding edge 72a in a direction transverse to the inlet direction 20a of the packaging material web 14a and transverse to the transport direction 38a of the packaging material tube 16a.
- the folded edge 72a extends at least substantially perpendicular to the inlet direction 20a of the packaging material web 14a and to the transport direction 38a of the packaging material tube 16a.
- the folding edge 72a and/or at least one further folding edge 110a of the molding unit 12a are intended to generate a homogeneous material tension in the packaging material 46a.
- the mold guide unit 18a is preferably intended to hold the packaging material tube 16a at least essentially perpendicular to the inlet direction 20a of the packaging material web 14a on the molding unit 12a, in particular along the transport direction 38a of the packaging material tube 16a, while maintaining the flow from the molding unit 12a, in particular from the folding edge 72a and / or to continue the homogeneous material tension generated by the further folding edge 110a.
- the mold guide unit 18a is along the Transport direction 38a of the packaging material tube 16a is arranged after the molding unit 12a and in particular in front of the longitudinal sealing unit 64a.
- the mold guide unit 18a is designed without rollers to deflect the packaging material tube 16a, in particular as a further mold shoulder.
- the mold guide unit 18a can have a geometry that is at least essentially analogous to a geometry of the mold unit 12a.
- the mold guide unit 18a is preferably designed, in particular arranged, separately from the mold unit 12a.
- the mold guide unit 18a is preferably designed as an independent component or as an independent assembly, in particular made up of two symmetrical components.
- the mold guide unit 18a is spaced apart from the packaging material tube 16a along a direction that is at least substantially perpendicular to the transport direction 38a of the packaging material tube 16a, in particular along the inlet direction 20a of the packaging material web 14a, and/or, in the present exemplary embodiment by way of example and, along the transport direction 38a of the packaging material tube 16a Molding unit 12a arranged.
- the mold guide unit 18a is designed in one piece with the mold unit 12a, in particular as a mold guide extension of the mold unit 12a.
- the horizontal forming device 10a preferably comprises at least one support surface 22a, in particular a worktop, on which products 24a to be packaged can be transported, the molding unit 12a and the mold guide unit 18a being arranged on sides 26a, 28a of the support surface 22a facing away from one another.
- the support surface 22a preferably forms a piece of track on which the products 24a can be transported.
- the support surface 22a preferably extends at least substantially parallel to the transport direction 38a of the packaging material tube 16a.
- the product feed unit 60a, the longitudinal sealing unit 64a, in particular the sealing rollers 66a, 68a, and/or the transverse sealing unit 70a are arranged at least in sections within the support surface 22a and extend/extend at least in sections through the support surface 22a.
- rotation axes 74a, 76a of the sealing rollers 66a, 68a of the longitudinal sealing unit 64a run at least substantially perpendicular to the support surface 22a.
- the molding unit is 12a is arranged on a side 26a of the support surface 22a, on which the products 24a can be transported and on which in particular the packaging material unwinding unit 54a and the packaging material supply unit 58a are arranged.
- the mold guide unit 18a is preferably arranged on a further side 28a of the support surface 22a, on which in particular the longitudinal sealing unit 64a is at least substantially parallel to the axes of rotation 74a, 76a of the sealing rollers 66a, at least to a large extent, in particular more than 50% of a maximum extent of the longitudinal sealing unit 64a , 68a, is arranged.
- the mold guide unit 18a can be coupled to the support surface 22a at least in sections.
- the packaging material tube 16a extends at least in sections through the support surface 22a, in particular onto the further side 28a of the support surface 22a.
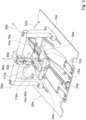
- FIG 3 shows part of the packaging machine 50a Figure 1 in a schematic perspective view.
- the horizontal forming device 10a preferably has at least one, in particular U-shaped, product and/or packaging material guide tunnel 78a, which is intended to support the packaging material tube 16a.
- the product and/or packaging material guide tunnel 78a is arranged in particular on the side 26a of the support surface 22a facing the molding unit 12a, in particular fastened to the support surface 22a.
- the product and/or packaging material guide tunnel 78a extends in particular along the transport direction 38a of the packaging material tube 16a from at least in front of the molding unit 12a to the molding unit 12a, preferably to the molding guide unit 18a and particularly preferably to the first pair of sealing rollers 66a of the longitudinal sealing unit 64a.
- the product and/or packaging material guide tunnel 78a has a cross section that is at least substantially analogous to a cross section of products 24a to be packaged, in particular a slightly larger cross section than the products 24a to be packaged.
- the products 24a can be transported within the product and/or packaging material guide tunnel 78a.
- the molding unit 12a is intended to shape the packaging material tube 16a at least in sections around the product and/or packaging material guide tunnel 78a, in particular around outer edges of the product and/or packaging material guide tunnel 78a.
- the product and/or packaging material guide tunnel 78a is intended to support the packaging material tube 16a, in particular in addition to the mold guide unit 18a.
- the horizontal forming device 10a and the packaging machine 50a are designed free of the product and/or packaging material guide tunnel 78a.
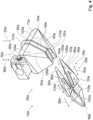
- Figure 4 shows a part of the horizontal forming device 10a of the packaging machine 50a Figure 1 in another schematic perspective view.
- the molding unit 12a preferably has at least two mold contour edges 80a, which extend from the folding edge 72a transversely to the folding edge 72a, in particular in a V-shape.
- the packaging material web 14a can be formed around the mold contour edges 80a and around the further folding edge 110a to form the packaging material tube 16a.
- the mold contour edges 80a preferably extend along a running direction of the packaging material 46a and/or along an outer contour of the supplied products 24a from the folded edge 72a to the further folded edge 110a, in particular to a mold tunnel 82a of the molding unit 12a, which is intended to hold the packaging material tube 16a along the transport direction 38a of the packaging material tube 16a.
- a longitudinal axis 84a of the mold tunnel 82a runs at least substantially parallel to the transport direction 38a of the packaging material tube 16a.
- the shape guide unit 18a comprises at least one, in particular three-dimensional, shape guide contour 86a, which is intended to support the guided packaging material tube 16a, in particular at least one outer edge of the packaging material tube 16a, in particular to achieve maintenance of the homogeneous material tension.
- the mold guide unit 18a has at least two mold guide contours 86a, which in particular are mirror-symmetrical about an imaginary plane of symmetry, which extends at least substantially parallel to the transport direction 38a of the packaging material tube 16a, in which in particular the transport direction 38a of the packaging material tube 16a runs, and which is at least in Extending essentially perpendicular to the folding edge 72a of the molding unit 12a, are arranged.
- the mold guide unit 18a is designed to be mirror-symmetrical, in particular around the imaginary plane of symmetry.
- the mold guide unit 18a and/or the mold unit 12a are/is designed asymmetrically.
- the horizontal forming device 10a preferably comprises at least one adjustment unit 30a, 32a, which is intended to adjustably mount the forming unit 12a and the forming guide unit 18a to realize different packaging material tube geometries, in particular in different adjustment planes.
- the horizontal forming device 10a preferably comprises at least two adjustment units 30a, 32a, with one adjustment unit 30a being intended to adjustably mount the forming unit 12a, and another adjustment unit 32a being intended to adjustably mount the molding guide unit 18a.
- different packaging material tube geometries may be required for packaging different products 24a.
- the packaging machine 50a is intended for packaging different products 24a, which in particular have different dimensions.
- packaging material tube geometries for packaging different products 24a which have different maximum extensions at least substantially perpendicular to the support surface 22a, in particular different heights, and/or the different maximum extensions at least substantially parallel to the support surface 22a and at least substantially perpendicular to the Transport direction 38a of the packaging material tube 16a, in particular different widths, are required.
- a maximum extension of the packaging material tube 16a is/is at least essentially perpendicular to the support surface 22a, in particular a height of the packaging material tube 16a, and/or a maximum extent of the packaging material tube 16a is at least essentially parallel to the support surface 22a and at least essentially perpendicular to the transport direction 38a of the packaging material tube 16a, in particular a width of the packaging material tube 16a, adjustable.
- the shape guide unit 18a can be adjustable by means of the further adjustment unit 32a to correct uneven tension conditions in the packaging material 46a.
- the molding unit 12a is adjustable in at least one adjustment plane extending on the side 26a of the support surface 22a facing the molding unit 12a.
- the mold guide unit 18a is adjustable in at least one further adjustment plane extending on the further side 28a of the support surface 22a facing the mold guide unit 18a.
- the mold unit 12a and/or the mold guide unit 18a are/are mounted adjustably as a whole component or as a whole assembly.
- the mold unit 12a and/or the mold guide unit 18a are adjustable in themselves, in particular individual components of the mold unit 12a relative to one another and/or individual components of the mold guide unit 18a relative to one another.
- the at least one setting unit 30a, 32a in particular the setting units 30a, 32a, is/are intended to mount the mold unit 12a and the mold guide unit 18a so that they can be adjusted relative to one another.
- the setting units 30a, 32a are intended to mount the mold unit 12a and the mold guide unit 18a as a whole component or as a whole assembly so that they can be adjusted relative to one another.
- the setting units 30a, 32a are preferably intended to mount the mold unit 12a and the mold guide unit 18a in a linearly movable and/or pivoting manner.
- the adjustment unit 30a is intended to support the molding unit 12a, in particular for adjusting a height of the packaging material tube 16a, in an at least linearly movable manner along an adjustment direction 88a that runs at least substantially perpendicular to the support surface 22a.
- the adjustment unit 30a comprises at least one linear guide 90a, which is intended to support the molding unit 12a in a linearly movable manner along the adjustment direction 88a.
- the adjustment unit 30a comprises at least one further linear guide 112a, which is intended to support the molding unit 12a in a linearly movable manner along a further adjustment direction 114a which runs at least essentially perpendicular to the adjustment direction 88a and at least essentially parallel to the transport direction 38a of the packaging material tube 16a (cf . Figure 3 ).
- the further adjustment unit 32a is intended to move the mold guide unit 18a at least linearly along at least one at least substantially parallel to the support surface 22a, in particular transverse to the transport direction 38a of the packaging material tube 16a, extending adjustment direction 92a, 116a.
- the setting units 30a, 32a are preferably designed as manual setting units for manual adjustment of the mold unit 12a and the mold guide unit 18a, in particular relative to one another.
- at least one of the adjustment units 30a, 32a has at least one automatic adjustment element, in particular a servomotor, which is provided for automatic adjustment of the mold unit 12a and/or the mold guide unit 18a.
- the at least one adjustment unit 30a, 32a in particular the adjustment units 30a, 32a, is/are intended to mount at least two mold legs 34a, 36a of the mold unit 12a and/or the mold guide unit 18a so that they can be adjusted relative to one another.
- the mold unit 12a has at least two mold legs 34a, which are mounted so that they can be adjusted relative to one another, in particular so that they can be moved linearly and/or pivotally.
- the mold legs 34a of the molding unit 12a are mounted so that they are at least linearly movable relative to one another, in particular along a direction that is at least substantially parallel to the folded edge 72a, in particular to a folded edge running surface.
- the adjustment unit 30a comprises at least one transverse bearing element 94a, which is intended to support the mold legs 34a of the mold unit 12a so that they can move at least linearly relative to one another.
- the mold legs 34a of the molding unit 12a jointly form the folded edge 72a, in particular the folded edge running surface.
- the mold legs 34a of the molding unit 12a are mounted to be movable toward and away from one another, in particular along the direction that runs at least substantially parallel to the folded edge 72a, in particular to adjust a width of the packaging material tube 16a.
- the mold legs 34a of the molding unit 12a together form the molding tunnel 82a of the molding unit 12a.
- each mold leg 34a of the molding unit 12a forms at least one mold contour edge 80a of the molding unit 12a.
- the adjustment unit 30a preferably has at least one intermediate element 96a, in particular a plurality of intermediate elements 96a, to fill a space between the two mold legs 34a of the mold unit 12a that move away from one another, in particular to ensure different product widths.
- the mold guide unit 18a has at least two mold legs 36a, which are mounted so that they can be adjusted relative to one another, in particular so that they can be moved linearly and/or pivotally.
- the further adjustment unit 32a which is provided for adjustable mounting of the mold guide unit 18a, can be designed in an alternative embodiment at least essentially analogous to the adjustment unit 30a, which is provided for adjustable storage of the mold unit 12a.
- the mold legs 36a of the mold guide unit 18a are mounted so that they can move at least linearly relative to one another.
- the further adjustment unit 32a is intended to mount the mold legs 36a of the mold guide unit 18a in a linearly movable manner along different, in particular transverse, adjustment directions 92a, 116a, in particular to ensure different product widths.
- the adjustment directions 92a, 116a run in a common plane, in particular extending at least substantially parallel to the support surface 22a, and in particular include equal angles with the transport direction 38a of the packaging material tube 16a.
- the mold legs 36a of the mold guide unit 18a can be mounted so that they can be at least pivotally movable relative to one another, in particular in a pivot plane that extends at least substantially parallel to the support surface 22a, in particular to adjust the width of the packaging material tube 16a.
- the mold legs 36a of the mold guide unit 18a can be pivotally mounted on an end region 98a of the mold legs 36a of the mold guide unit 18a that is remote from the mold unit 12a along the transport direction 38a of the packaging material tube 16a.
- the end region 98a of the mold legs 36a of the mold guide unit 18a can be formed, in particular mounted, separately from a remaining region of the mold guide unit 18a, in particular separated from the remaining region along a separating cut 118a.
- each mold leg 36a of the mold guide unit 18a forms at least one mold guide contour 86a of the mold guide unit 18a.
- the mold legs 36a of the mold guide unit 18a are arranged, in particular mounted, in mirror symmetry to one another around the imaginary plane of symmetry.
- the mold legs 36a of the mold guide unit 18a preferably form a V-shaped tapering guide region 40a in the transport direction 38a of the packaging material tube 16a, which is intended to bring together seam regions of the packaging material tube 16a that are to be sealed with one another.
- the guide area 40a is intended to bring together longitudinal sealing seam areas of the packaging material tube 16a that are to be sealed with one another.
- the mold legs 36a of the mold guide unit 18a in an end region 100a facing the mold unit 12a have a greater distance from one another along a direction that is at least substantially parallel to the support surface 22a and at least substantially perpendicular to the transport direction 38a of the packaging material tube 16a than in that of the mold unit 12a facing away from the end region 98a.
- the seam areas of the packaging material tube 16a are in particular areas in which the packaging material 46a, in particular the packaging paper, is sealed, in particular to create a sealing seam.
- the guide area 40a is intended to bring the seam areas together in such a way that the seam areas can be transported between two sealing rollers 66a, 68a of the pairs of sealing rollers 66a, 68a to form a seal.
- the guide region 40a preferably opens in the end region 98a facing away from the mold unit 12a into a support contour 102a formed by the mold legs 36a of the mold guide unit 18a, which is intended to support the packaging material tube 16a, in particular the joined seam regions, in particular during further transport to the longitudinal sealing unit 64a.
- FIG. 5 shows part of a first alternative horizontal forming device 10b in a schematic perspective view.
- the horizontal forming device 10b in particular comprises at least one forming unit 12b and at least one forming guide unit 18b.
- the horizontal shaping device 10b preferably comprises at least one heating unit 42b, which is intended to heat the shaping unit 12b and/or the shape guiding unit 18b at least in sections, in particular to introduce heat into a seam area, in particular a packaging material.
- the heating unit 42b is intended to enable a prior heat input into the packaging material, in particular into the packaging paper, during a sealing, in particular a longitudinal sealing, of the packaging material, in particular a packaging paper.
- the heating unit 42b is intended to seal the packaging material, in particular the packaging paper, in particular on the form guide unit 18b, in particular as an alternative to sealing by a longitudinal sealing unit of a packaging machine, and/or to ensure increased heat input, in particular in an area of a support contour 102b of the mold guide unit 18b.
- the heating unit 42b can in particular be designed as a heating coil, as a heating cartridge, as a heating plate, as a thick-film heating element or as another heating unit that appears sensible to a person skilled in the art.
- the heating unit 42b is preferably arranged on the mold unit 12b and/or on the mold guide unit 18b, and is in particular in direct contact with the mold unit 12b and/or the mold guide unit 18b.
- the horizontal molding device 10b can have a plurality of heating units 42b, wherein at least one heating unit 42b can be assigned to the molding unit 12b and at least one further heating unit 42b can be assigned to the mold guide unit 18b.
- the heating unit 42b is arranged on a side of the mold unit 12b and/or the mold guide unit 18b facing away from a contact surface 104b with the packaging material, in particular with the packaging paper.
- the horizontal forming device 10b has, for example, a single heating unit 42b, which is located on the forming unit 12b, in particular on the contact surface 104b facing away from the packaging material Side of the molding unit 12b, is arranged, in particular in direct contact with the molding unit 12b.
- a heater which is arranged parallel to a surface 120b of the molding unit 12b, in particular at a distance from the molding unit 12b, is conceivable, which heats the packaging material on an inside.
- the molding unit 12b and/or the molding guide unit 18b are intended to transfer thermal energy absorbed by the heating unit 42b to the packaging material, in particular to the packaging paper.
- the mold unit 12b, in particular the mold legs 34b of the mold unit 12b, and/or the mold guide unit 18b, in particular the mold legs 36b of the mold guide unit 18b, in the present exemplary embodiment by way of example at least the mold unit 12b are made of a thermally conductive material, in particular made of a metal, educated.
- the molding unit 12b and/or the molding guide unit 18b, in the present exemplary embodiment for example the molding unit 12b, on the contact surface 104b with the packaging material, in particular with the packaging paper, is/is intended to transfer thermal energy provided by the heating unit 42b to the packaging material, in particular in the seam areas.
- at least one sealing layer of the packaging paper can be activated by applying heat to the seam areas.
- FIG. 6 shows part of a second alternative horizontal forming device 10c in a schematic perspective view.
- the horizontal molding device 10c in particular includes at least one molding unit 12c and at least one molding guide unit 18c.
- the horizontal molding device 10c preferably comprises at least one air pressure unit 44c, which is intended to exert a negative pressure and/or an excess pressure on a packaging material at the molding unit 12c and/or at the mold guide unit 18c.
- the horizontal forming device 10c has, for example, two air pressure units 44c, with one of the air pressure units 44c being intended to exert a negative pressure and/or an excess pressure on the packaging material on a mold leg 36c of the mold guide unit 18c.
- the air pressure units 44c can in particular be used as blowers, as vacuum cleaners or be designed as other air pressure units that appear useful to a person skilled in the art.
- the horizontal molding device 10c can have a plurality of air pressure units 44c, wherein at least one air pressure unit 44c can be assigned to the molding unit 12c and at least one further air pressure unit 44c can be assigned to the mold guide unit 18c.
- the air pressure units 44c are arranged on a side of the molding unit 12c and/or the molding guide unit 18c, in the present exemplary embodiment for example the molding guide unit 18c, facing away from a contact surface 106c with the packaging material, in particular with a packaging paper.
- the mold unit 12c, in particular mold legs 34c of the mold unit 12c, and/or the mold guide unit 18c, in particular the mold legs 36c of the mold guide unit 18c, in the present exemplary embodiment for example the mold guide unit 18c are formed at least in sections perforated, in particular made of a porous material.
- the mold legs 36c of the mold guide unit 18c have a perforation 108c.
- air from an air flow generated by the air pressure units 44c can flow at least in sections through the mold unit 12c and/or the mold guide unit 18c, in the present exemplary embodiment for example through the mold guide unit 18c.
- the air pressure units 44c are provided to generate a negative pressure for suction of the packaging paper to the molding unit 12c and/or to the molding guide unit 18c, in the present exemplary embodiment, for example, to the molding guide unit 18c, in particular to achieve a low-crease contact of the packaging paper on the Mold unit 12c and/or on the mold guide unit 18c, in the present exemplary embodiment for example on the mold guide unit 18c.
- the air pressure units 44c are intended to generate an overpressure to form an air cushion on the molding unit 12c and/or on the molding guide unit 18c, in the present exemplary embodiment for example on the molding guide unit 18c, in particular to realize a low-friction transport of the packaging paper along the Mold unit 12c and/or along the mold guide unit 18c, in the present exemplary embodiment, for example, along the mold guide unit 18c.
- the air pressure units 44c can be switched between generating a negative pressure and generating an overpressure, in particular depending on an application situation, for example depending on the packaging material used.
- FIG. 7 shows part of a third alternative horizontal forming device 10d in a schematic perspective view.
- the horizontal forming device 10d comprises at least one forming unit 12d and at least one forming guide unit 18d.
- the horizontal forming device 10d preferably comprises at least one driven pressure unit 48d, in particular a pressure roller, which is intended to apply a pressure force to a packaging material against the mold guide unit 18d.
- the horizontal forming device 10d preferably comprises the at least one driven pressure unit 48d as an alternative or in addition, in the present exemplary embodiment as an alternative, to an air pressure unit assigned to the mold guiding unit 18d.
- the horizontal forming device 10d preferably comprises at least two driven pressure units 48d, with at least one driven pressure unit 48d being assigned to a mold leg 36d of the mold guide unit 18d, in particular being intended to apply a pressure force to the packaging material against the mold leg 36d.
- the horizontal forming device 10d includes at least one additional driven pressure unit 48d, in particular an additional pressure roller, which is intended to apply a pressure force to the packaging material against the molding unit 12d.
- the driven pressure units 48d are preferably designed as pressure rollers which can be driven to perform rotational movements, in particular to transport a packaging material tube along a transport direction 38d of the packaging material tube.
- the driven pressure units 48d are intended to guide the packaging material tube between the driven pressure units 48d and the mold guide unit 18d, in particular the mold legs 36d of the mold guide unit 18d.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Package Closures (AREA)
- Folding Of Thin Sheet-Like Materials, Special Discharging Devices, And Others (AREA)
Description
- Aus
US 5 235 792 A sowie ausJP H10-16906 A - Ferner sind aus
EP 1 364 876 A1 ,JP H06-312 710 A US 4 520 615 A ebenfalls bereits Horizontalformvorrichtungen bekannt. - Die Erfindung geht aus von einer Horizontalformvorrichtung, insbesondere für horizontale Schlauchbeutelmaschinen, mit zumindest einer, insbesondere rollenfreien, Formeinheit, insbesondere einer Formschulter, die dazu vorgesehen ist, eine Verpackungsmaterialbahn, insbesondere eine Papierbahn, zu einem Verpackungsmaterialschlauch zu formen, wobei die Formeinheit zumindest eine Faltkante aufweist, um die die Verpackungsmaterialbahn umlenkbar ist, und mit zumindest einer Formführungseinheit, insbesondere einer weiteren Formschulter, die dazu vorgesehen ist, den Verpackungsmaterialschlauch quer zu einer Einlaufrichtung der Verpackungsmaterialbahn an der Formeinheit unter Erhalt einer von der Formeinheit erzeugten, insbesondere homogenen, Materialspannung weiterzuführen.
- Es wird vorgeschlagen, dass die Horizontalformvorrichtung zumindest eine Auflagefläche, insbesondere eine Arbeitsplatte, umfasst, auf der zu verpackende Produkte transportierbar sind, wobei die Formeinheit und die Formführungseinheit auf voneinander abgewandten Seiten der Auflagefläche angeordnet sind, wobei die Formführungseinheit zumindest eine Formführungskontur umfasst, die dazu vorgesehen ist, den geführten Verpackungsmaterialschlauch zu einer Realisierung einer Aufrechterhaltung der homogenen Materialspannung zu stützen.
- Vorzugsweise umfasst eine Verpackungsmaschine, insbesondere eine horizontale Schlauchbeutelmaschine, die Horizontalformvorrichtung. Insbesondere ist die Horizontalformvorrichtung dazu vorgesehen, ein Verpackungsmaterial, insbesondere den Verpackungsmaterialschlauch, entlang einer horizontalen, insbesondere entlang einer zumindest im Wesentlichen senkrecht zu einer Gravitationskraftwirkrichtung verlaufenden, Transportrichtung zu führen. Der Ausdruck "im Wesentlichen senkrecht" soll insbesondere eine Ausrichtung einer Richtung relativ zu einer Bezugsrichtung definieren, wobei die Richtung und die Bezugsrichtung, insbesondere in einer Projektionsebene betrachtet, einen Winkel von 90° einschließen und der Winkel eine maximale Abweichung von insbesondere kleiner als 8°, vorteilhaft kleiner als 5° und besonders vorteilhaft kleiner als 2° aufweist. Unter "vorgesehen" soll insbesondere speziell programmiert, speziell ausgelegt und/oder speziell ausgestattet verstanden werden. Darunter, dass ein Objekt zu einer bestimmten Funktion vorgesehen ist, soll insbesondere verstanden werden, dass das Objekt diese bestimmte Funktion in zumindest einem Anwendungs- und/oder Betriebszustand erfüllt und/oder ausführt.
- Vorzugsweise ist die Horizontalformvorrichtung zumindest zu einer Formung und/oder Führung einer Verpackungsmaterialbahn vorgesehen, wobei das Verpackungsmaterial bevorzugt als ein Papier ausgebildet ist. Insbesondere ist die Verpackungsmaterialbahn als eine Papierbahn ausgebildet. Vorzugsweise kann die Horizontalformvorrichtung zusätzlich oder zumindest alternativ zu einer Formung und/oder Führung einer Verpackungsmaterialbahn vorgesehen sein, wobei das Verpackungsmaterial verschieden von einem Papier, beispielsweise als ein Kunststoff, ausgebildet ist. Insbesondere kann die Verpackungsmaterialbahn alternativ aus einem Kunststoff ausgebildet sein. Das Verpackungsmaterial ist insbesondere zu einer Verpackung, insbesondere zu einer Umhüllung, von Produkten, insbesondere von Lebensmittelprodukten, vorgesehen. Das Verpackungsmaterial ist bevorzugt als Verpackungspapier ausgebildet. Unter einer "Verpackungsmaterialbahn" soll insbesondere eine ebene, insbesondere zweidimensionale, Konfiguration des Verpackungsmaterials, insbesondere des Verpackungspapiers, verstanden werden. Vorzugsweise umfasst die Verpackungsmaschine zumindest eine Verpackungsmaterialabwickeleinheit, die dazu vorgesehen ist, das Verpackungsmaterial, insbesondere als eine Verpackungsmaterialrolle, aufzunehmen. Vorzugsweise ist die Verpackungsmaterialabwickeleinheit dazu vorgesehen, das Verpackungsmaterial als eine Verpackungsmaterialbahn abzuwickeln, insbesondere einer Verpackungsmaterialzuführeinheit der Verpackungsmaschine zuzuführen. Die Verpackungsmaterialzuführeinheit ist insbesondere dazu vorgesehen, der Horizontalformvorrichtung, insbesondere der Formeinheit, die Verpackungsmaterialbahn zuzuführen. Die Verpackungsmaterialzuführeinheit kann eine Mehrzahl von, insbesondere einem Fachmann bekannten, Komponenten, wie beispielsweise zumindest einen Schwinghebel, zumindest einen Zentriertaster, zumindest eine Bahnkantensteuerung und/oder zumindest eine Druckeinheit zu einem Bedrucken des Verpackungsmaterials, umfassen.
- Unter einem "Verpackungsmaterialschlauch" soll insbesondere eine, insbesondere zumindest quer zu einer Bahnebene der Verpackungsmaterialbahn, umgeformte, insbesondere dreidimensionale, Konfiguration des Verpackungsmaterials, insbesondere des Verpackungspapiers, verstanden werden. Insbesondere ist der Verpackungsmaterialschlauch dazu vorgesehen, zu verpackende Produkte zu umhüllen. Insbesondere weist die Verpackungsmaschine zumindest eine Produktzuführeinheit, insbesondere ein Förderband, eine Mitnehmerkette o. dgl., auf, die dazu vorgesehen ist, die zu verpackenden Produkte zu einer Umhüllung durch den Verpackungsmaterialschlauch in einen Bereich der Horizontalformvorrichtung, insbesondere der Formeinheit, zu transportieren. Vorzugsweise verläuft eine Transportrichtung der Produkte zumindest im Wesentlichen parallel zu einer Transportrichtung des Verpackungsmaterialschlauchs. Unter "im Wesentlichen parallel" soll insbesondere eine Ausrichtung einer Richtung relativ zu einer Bezugsrichtung, insbesondere in einer Ebene, verstanden werden, wobei die Richtung gegenüber der Bezugsrichtung eine Abweichung insbesondere kleiner als 8°, vorteilhaft kleiner als 5° und besonders vorteilhaft kleiner als 2° aufweist. Vorzugsweise ist die Produktzuführeinheit entlang der Transportrichtung des Verpackungsmaterialschlauchs vor der Horizontalformvorrichtung, insbesondere vor der Formeinheit, angeordnet.
- Vorzugsweise umfasst die Verpackungsmaschine zumindest eine Längssiegeleinheit, die dazu vorgesehen ist eine, insbesondere zumindest im Wesentlichen parallel zu der Transportrichtung des Verpackungsmaterialschlauchs verlaufende, Längssiegelnaht des Verpackungsmaterialschlauchs zu erstellen, insbesondere durch einen Wärmeeintrag in das Verpackungsmaterial und/oder durch einen Druck auf das Verpackungsmaterial. Die Längssiegeleinheit ist entlang der Transportrichtung des Verpackungsmaterialschlauchs nach der Horizontalformvorrichtung, insbesondere nach der Formführungseinheit, angeordnet. insbesondere umfasst die Längssiegeleinheit zumindest ein Paar von, insbesondere mit einem Profil versehenen, mit Druck beaufschlagbaren und/oder beheizbaren, Siegelrollen, die dazu vorgesehen sind, insbesondere durch eine Rotation, den Verpackungsmaterialschlauch zu transportieren. Vorzugsweise umfasst die Längssiegeleinheit eine Mehrzahl von Paaren von Siegelrollen, wobei zumindest ein erstes entlang der Transportrichtung des Verpackungsmaterialschlauchs nach der Horizontalformvorrichtung angeordnetes Paar von Siegelrollen beheizungsfrei, insbesondere zu einem beheizungsfreien Transport des Verpackungsmaterialschlauchs, ausgebildet ist. Vorzugsweise umfasst die Verpackungsmaschine zumindest eine Quersiegeleinheit, die dazu vorgesehen ist, insbesondere nach jeweils einem Produkt, Quersiegelnähte des Verpackungsmaterialschlauchs, die insbesondere zumindest im Wesentlichen senkrecht zu der Transportrichtung des Verpackungsmaterialschlauchs verlaufen, zu erstellen, insbesondere durch gezielten Druck auf das Verpackungsmaterial und/oder durch einen Wärmeeintrag in das Verpackungsmaterial. Insbesondere ist die Quersiegeleinheit dazu vorgesehen, den Verpackungsmaterialschlauch in einzelne Verpackungen, die insbesondere jeweils ein Produkt umschließen, zu vereinzeln. Die Quersiegeleinheit ist entlang der Transportrichtung des Verpackungsmaterialschlauchs nach der Längssiegeleinheit angeordnet.
- Die Formeinheit ist vorzugsweise dazu vorgesehen, die Verpackungsmaterialbahn umzulenken. Insbesondere ist die Verpackungsmaterialzuführeinheit dazu vorgesehen, der Formeinheit die Verpackungsmaterialbahn entlang einer quer, insbesondere zumindest im Wesentlichen senkrecht, zu der Transportrichtung des Verpackungsmaterialschlauchs verlaufenden Richtung zuzuführen. Die Formeinheit weist zumindest eine Faltkante auf, um die die Verpackungsmaterialbahn umlenkbar ist. Bevorzugt ist die Faltkante als eine Schulterkante und die Formeinheit als eine Formschulter ausgebildet. Insbesondere ist die Formeinheit frei von Rollen zu einer Umlenkung der Verpackungsmaterialbahn ausgebildet. Vorzugsweise ist die Formeinheit dazu vorgesehen, die Verpackungsmaterialbahn an der Faltkante in eine Richtung quer zu der Einlaufrichtung der Verpackungsmaterialbahn und quer zu der Transportrichtung des Verpackungsmaterialschlauchs umzulenken. Insbesondere erstreckt sich die Faltkante zumindest im Wesentlichen senkrecht zu der Einlaufrichtung der Verpackungsmaterialbahn und zu der Transportrichtung des Verpackungsmaterialschlauchs. Insbesondere ist die Faltkante dazu vorgesehen, eine homogene Materialspannung in dem Verpackungsmaterial zu erzeugen. Die Formeinheit weist vorzugsweise zumindest zwei Formkonturkanten, die sich ausgehend von der Faltkante quer zu der Faltkante, insbesondere V-förmig, erstrecken, auf. Insbesondere ist die Verpackungsmaterialbahn um die Formkonturkanten zu dem Verpackungsmaterialschlauch umformbar. Vorzugsweise erstrecken sich die Formkonturkanten entlang einer Laufrichtung des Verpackungsmaterials und/oder entlang einer Außenkontur der zugeführten Produkte von der Faltkante bis zu einem Formtunnel der Formeinheit, der dazu vorgesehen ist, den Verpackungsmaterialschlauch entlang der Transportrichtung des Verpackungsmaterialschlauchs zu führen. Insbesondere verläuft eine Längsachse des Formtunnels zumindest im Wesentlichen parallel zu der Transportrichtung des Verpackungsmaterialschlauchs.
- Die Formführungseinheit ist bevorzugt dazu vorgesehen, den Verpackungsmaterialschlauch zumindest im Wesentlichen senkrecht zu der Einlaufrichtung der Verpackungsmaterialbahn an der Formeinheit, insbesondere entlang der Transportrichtung des Verpackungsmaterialschlauchs, unter Erhalt der von der Formeinheit, insbesondere von der Faltkante, erzeugten homogenen Materialspannung weiterzuführen. Insbesondere ist die Formführungseinheit entlang der Transportrichtung des Verpackungsmaterialschlauchs nach der Formeinheit und insbesondere vor der Längssiegeleinheit angeordnet. Die Formführungseinheit umfasst zumindest eine, insbesondere dreidimensionale, Formführungskontur, die dazu vorgesehen ist, den geführten Verpackungsmaterialschlauch, insbesondere zumindest eine Außenkante des Verpackungsmaterialschlauchs, zu stützen, zu einer Realisierung einer Aufrechterhaltung der homogenen Materialspannung. Vorzugsweise weist die Formführungseinheit zumindest zwei Formführungskonturen auf, die insbesondere spiegelsymmetrisch um eine gedachte Symmetrieebene, die sich zumindest im Wesentlichen parallel zu der Transportrichtung des Verpackungsmaterialschlauchs erstreckt, in der insbesondere die Transportrichtung des Verpackungsmaterialschlauchs verläuft, und die sich zumindest im Wesentlichen senkrecht zu der Faltkante der Formeinheit erstreckt, angeordnet sind. Vorzugsweise ist die Formführungseinheit, insbesondere um die gedachte Symmetrieebene, spiegelsymmetrisch ausgebildet. Alternativ ist vorstellbar, dass die Formführungseinheit und/oder die Formeinheit asymmetrisch ausgebildet sind/ist. Vorzugsweise ist die Formführungseinheit frei von Rollen zu einer Umlenkung des Verpackungsmaterialschlauchs, insbesondere als eine weitere Formschulter, ausgebildet. Insbesondere kann die Formführungseinheit eine zu einer Geometrie der Formeinheit zumindest im Wesentlichen analoge Geometrie aufweisen.
- Die Auflagefläche bildet vorzugsweise eine Stückbahn aus, auf der die Produkte transportierbar sind. Die Auflagefläche erstreckt sich vorzugsweise zumindest im Wesentlichen parallel zu der Transportrichtung des Verpackungsmaterialschlauchs. Vorzugsweise sind/ist die Produktzuführeinheit, die Längssiegeleinheit, insbesondere die Siegelrollen, und/oder die Quersiegeleinheit zumindest abschnittsweise innerhalb der Auflagefläche angeordnet, erstrecken/erstreckt sich zumindest abschnittsweise durch die Auflagefläche hindurch. Insbesondere verlaufen Rotationsachsen der Siegelrollen der Längssiegeleinheit zumindest im Wesentlichen senkrecht zu der Auflagefläche. Vorzugsweise ist die Formeinheit auf einer Seite der Auflagefläche angeordnet, auf der die Produkte transportierbar sind und auf der insbesondere die Verpackungsmaterialabwickeleinheit und die Verpackungsmaterialzuführeinheit angeordnet sind. Die Formführungseinheit ist vorzugsweise auf einer weiteren Seite der Auflagefläche angeordnet, auf der insbesondere die Längssiegeleinheit zumindest zu einem Großteil, insbesondere mehr als 50 % einer maximalen Erstreckung der Längssiegeleinheit zumindest im Wesentlichen parallel zu den Rotationsachsen der Siegelrollen, angeordnet ist. Insbesondere kann die Formführungseinheit zumindest abschnittsweise mit der Auflagefläche gekoppelt sein. Insbesondere erstreckt sich der Verpackungsmaterialschlauch zumindest abschnittsweise durch die Auflagefläche hindurch, insbesondere auf die weitere Seite der Auflagefläche.
- Durch die erfindungsgemäße Ausgestaltung der Horizontalformvorrichtung kann vorteilhaft der Verpackungsmaterialschlauch auf zwei voneinander abgewandten Seiten der Auflagefläche präzise geführt werden. Es kann vorteilhaft eine präzise Umformung einer Verpackungsmaterialbahn zu einem Verpackungsmaterialschlauch ermöglicht werden. Vorteilhaft können Verpackungsmaterialbahnen aus empfindlichen, insbesondere reißanfällige und/oder sehr dünne, Materialien, insbesondere aus Papier, zu Verpackungsmaterialschläuchen umgeformt werden. Es können vorteilhaft zumindest im Wesentlichen faltenfreie Verpackungsschläuche hergestellt werden. Es kann eine vorteilhaft kompakt ausgestaltete Horizontalformvorrichtung bereitgestellt werden.
- Des Weiteren wird vorgeschlagen, dass die Formführungseinheit getrennt von der Formeinheit ausgebildet, insbesondere angeordnet, ist. Vorzugsweise ist die Formführungseinheit als ein eigenständiges Bauteil oder als eine eigenständige Baugruppe, insbesondere aus zwei symmetrischen Bauteilen, ausgebildet. Insbesondere ist die Formführungseinheit entlang einer zumindest im Wesentlichen senkrecht zu der Transportrichtung des Verpackungsmaterialschlauchs verlaufenden Richtung, insbesondere entlang der Einlaufrichtung der Verpackungsmaterialbahn, und/oder entlang der Transportrichtung des Verpackungsmaterialschlauchs beabstandet von der Formeinheit angeordnet. Alternativ ist vorstellbar, dass die Formführungseinheit einteilig mit der Formeinheit, insbesondere als ein Formführungsfortsatz der Formeinheit, ausgebildet ist. Unter "einteilig" soll insbesondere in einem Stück geformt verstanden werden. Vorzugsweise wird dieses eine Stück aus einem einzelnen Rohling, einer Masse und/oder einem Guss, besonders bevorzugt in einem Spritzgussverfahren, insbesondere einem Ein- und/oder Mehrkomponenten-Spritzgussverfahren, hergestellt. Vorteilhaft kann eine präzise Führung des Verpackungsmaterialschlauchs über eine lange Strecke ermöglicht werden.
- Des Weiteren wird vorgeschlagen, dass die Horizontalformvorrichtung zumindest einen, insbesondere U-förmigen, Produkt- und/oder Verpackungsmaterialführungstunnel aufweist, der dazu vorgesehen ist, den Verpackungsmaterialschlauch zu stützen. Der Produkt- und/oder Verpackungsmaterialführungstunnel kann insbesondere auf der der Formeinheit zugewandten Seite der Auflagefläche angeordnet, insbesondere an der Auflagefläche befestigt, sein. Der Produkt- und/oder Verpackungsmaterialführungstunnel kann sich insbesondere entlang der Transportrichtung des Verpackungsmaterialschlauchs von zumindest vor der Formeinheit bis zur Formeinheit, bevorzugt bis zur Formführungseinheit und besonders bevorzugt bis zu dem ersten Paar von Siegelrollen der Längssiegeleinheit erstrecken. Vorzugsweise weist der Produkt- und/oder Verpackungsmaterialführungstunnel einen zumindest im Wesentlichen analog zu einem Querschnitt von zu verpackenden Produkten ausgebildeten Querschnitt, insbesondere einen leicht größeren Querschnitt als die zu verpackenden Produkte, auf. Insbesondere sind die Produkte innerhalb des Produkt- und/oder Verpackungsmaterialführungstunnels transportierbar. Vorzugsweise ist die Formeinheit dazu vorgesehen, den Verpackungsmaterialschlauch zumindest abschnittsweise um den Produkt- und/oder Verpackungsmaterialführungstunnel, insbesondere um Außenkanten des Produkt- und/oder Verpackungsmaterialführungstunnels, zu formen. Insbesondere ist der Produkt- und/oder Verpackungsmaterialführungstunnel dazu vorgesehen, den Verpackungsmaterialschlauch, insbesondere zusätzlich zu der Formführungseinheit, zu stützen. Alternativ ist denkbar, dass die Horizontalformvorrichtung und die Verpackungsmaschine frei von einem Produkt- und/oder Verpackungsmaterialführungstunnel ausgebildet sind. Vorteilhaft kann ein präzises Umschließen der Produkte ermöglicht werden.
- Weiterhin wird vorgeschlagen, dass die Horizontalformvorrichtung zumindest eine Einstelleinheit umfasst, die dazu vorgesehen ist, die Formeinheit und die Formführungseinheit zu einer Realisierung von unterschiedlichen Verpackungsmaterialschlauchgeometrien verstellbar zu lagern, insbesondere in unterschiedlichen Verstellebenen. Vorzugsweise umfasst die Horizontalformvorrichtung zumindest zwei Einstelleinheiten, wobei eine Einstelleinheit dazu vorgesehen ist, die Formeinheit verstellbar zu lagern, und wobei eine weitere Einstelleinheit dazu vorgesehen ist, die Formführungseinheit verstellbar zu lagern. Insbesondere können zu einer Verpackung von unterschiedlichen Produkten unterschiedliche Verpackungsmaterialschlauchgeometrien benötigt werden. Insbesondere ist die Verpackungsmaschine zu einer Verpackung von unterschiedlichen Produkten, die insbesondere unterschiedliche Abmessungen aufweisen, vorgesehen. Insbesondere können unterschiedliche Verpackungsmaterialschlauchgeometrien zur Verpackung von unterschiedlichen Produkten, die unterschiedliche maximale Erstreckungen zumindest im Wesentlichen senkrecht zu der Auflagefläche, insbesondere unterschiedliche Höhen, und/oder die unterschiedliche maximale Erstreckungen zumindest im Wesentlichen parallel zu der Auflagefläche und quer zu der Transportrichtung des Verpackungsmaterialschlauchs, insbesondere unterschiedliche Breiten, aufweisen, benötigt werden. Insbesondere sind/ist durch eine Verstellung der Formeinheit und/oder der Formführungseinheit eine maximale Erstreckung des Verpackungsmaterialschlauchs zumindest im Wesentlichen senkrecht zu der Auflagefläche, insbesondere eine Höhe des Verpackungsmaterialschlauchs, und/oder eine maximale Erstreckung des Verpackungsmaterialschlauchs zumindest im Wesentlichen parallel zu der Auflagefläche und quer zu der Transportrichtung des Verpackungsmaterialschlauchs, insbesondere eine Breite des Verpackungsmaterialschlauchs, einstellbar. Insbesondere kann die Formführungseinheit mittels der weiteren Einstelleinheit zu einer Korrektur ungleichmäßiger Spannungsverhältnisse in dem Verpackungsmaterial einstellbar sein.
- Vorzugsweise ist die Formeinheit in zumindest einer sich auf der der Formeinheit zugewandten Seite der Auflagefläche erstreckenden Verstellebene verstellbar gelagert. Vorzugsweise ist die Formführungseinheit in zumindest einer weiteren, sich auf der weiteren, der Formführungseinheit zugewandten Seite der Auflagefläche erstreckenden Verstellebene verstellbar gelagert. Insbesondere sind/ist die Formeinheit und/oder die Formführungseinheit als ganzes Bauteil oder als ganze Baugruppe verstellbar gelagert. Insbesondere sind/ist die Formeinheit und/oder die Formführungseinheit in sich selbst verstellbar, insbesondere einzelne Komponenten der Formeinheit relativ zueinander und/oder einzelne Komponenten der Formführungseinheit relativ zueinander. Es kann eine Horizontalformvorrichtung bereitgestellt werden, die eine vorteilhaft formatflexible Anpassung von einer Verpackungsmaterialschlauchgeometrie an unterschiedliche zu verpackende Produkte ermöglicht.
- Zudem wird vorgeschlagen, dass die zumindest eine Einstelleinheit, insbesondere die Einstelleinheiten, dazu vorgesehen ist/sind, die Formeinheit und die Formführungseinheit relativ zueinander verstellbar zu lagern. Insbesondere sind die Einstelleinheiten dazu vorgesehen, die Formeinheit und die Formführungseinheit als ganzes Bauteil oder als ganze Baugruppe relativ zueinander verstellbar zu lagern. Vorzugsweise sind die Einstelleinheiten dazu vorgesehen, die Formeinheit und die Formführungseinheit linearbeweglich und/oder schwenkbeweglich zu lagern. Vorzugsweise ist die Einstelleinheit dazu vorgesehen, die Formeinheit, insbesondere zu einer Einstellung einer Höhe des Verpackungsmaterialschlauchs, zumindest linearbeweglich entlang einer zumindest im Wesentlichen senkrecht zu der Auflagefläche verlaufenden Verstellrichtung zu lagern. Alternativ oder zusätzlich ist vorstellbar, dass die Einstelleinheit dazu vorgesehen ist, die Formeinheit linearbeweglich entlang einer zumindest im Wesentlichen senkrecht zu der Verstellrichtung und zumindest im Wesentlichen parallel zu der Transportrichtung des Verpackungsmaterialschlauchs verlaufenden weiteren Verstellrichtung zu lagern. Vorzugsweise ist die weitere Einstelleinheit dazu vorgesehen, die Formführungseinheit zumindest linearbeweglich entlang zumindest einer zumindest im Wesentlichen parallel zu der Auflagefläche, insbesondere quer zu der Transportrichtung des Verpackungsmaterialschlauchs, verlaufenden Verstellrichtung zu lagern. Vorzugsweise sind die Einstelleinheiten als manuelle Einstelleinheiten zu einer manuellen Verstellung der Formeinheit und der Formführungseinheit, insbesondere relativ zueinander, ausgebildet. Alternativ oder zusätzlich ist vorstellbar, dass zumindest eine der Einstelleinheiten zumindest ein automatisches Verstellelement, insbesondere einen Stellmotor, aufweist, das/der zu einer automatischen Verstellung der Formeinheit und/oder der Formführungseinheit vorgesehen ist. Vorteilhaft kann eine für unterschiedliche Produkte und/oder Verpackungsmaterialien optimierte Positionierung der Formeinheit und der Formführungseinheit relativ zueinander ermöglicht werden.
- Des Weiteren wird vorgeschlagen, dass die zumindest eine Einstelleinheit, insbesondere die Einstelleinheiten, dazu vorgesehen ist/sind, zumindest zwei Formschenkel der Formeinheit und/oder der Formführungseinheit relativ zueinander verstellbar zu lagern. Vorzugsweise weist die Formeinheit zumindest zwei Formschenkel auf, die relativ zueinander verstellbar, insbesondere linearbeweglich und/oder schwenkbeweglich, gelagert sind. Insbesondere sind die Formschenkel der Formeinheit relativ zueinander zumindest linearbeweglich, insbesondere entlang einer zumindest im Wesentlichen parallel zu der Faltkante, insbesondere zu einer Faltkantenlauffläche, verlaufenden Richtung, verstellbar gelagert. Insbesondere bilden die Formschenkel der Formeinheit die Faltkante, insbesondere die Faltkantenlauffläche, gemeinsam aus. Insbesondere sind die Formschenkel der Formeinheit, insbesondere entlang der zumindest im Wesentlichen parallel zu der Faltkante, insbesondere zu der Faltkantenlauffläche, verlaufenden Richtung, aufeinander zu und voneinander weg beweglich gelagert, insbesondere zu einer Einstellung einer Breite des Verpackungsmaterialschlauchs. Insbesondere bilden die Formschenkel der Formeinheit gemeinsam den Formtunnel der Formeinheit aus. Insbesondere bildet jeweils ein Formschenkel der Formeinheit jeweils zumindest eine Formkonturkante der Formeinheit aus. Die Einstelleinheit weist vorzugsweise zumindest ein Zwischenelement, insbesondere eine Mehrzahl von Zwischenelementen, zu einer Ausfüllung eines Raums zwischen den zwei voneinander wegbewegten Formschenkeln der Formeinheit auf, insbesondere zu einer Gewährleistung von unterschiedlichen Produktbreiten.
- Vorzugsweise weist die Formführungseinheit zumindest zwei Formschenkel auf, die relativ zueinander verstellbar, insbesondere linearbeweglich und/oder schwenkbeweglich, gelagert sind. Insbesondere kann die weitere Einstelleinheit, die zu einer verstellbaren Lagerung der Formführungseinheit vorgesehen ist, zumindest im Wesentlichen analog zu der Einstelleinheit, die zu einer verstellbaren Lagerung der Formeinheit vorgesehen ist, ausgebildet sein. Vorzugsweise sind die Formschenkel der Formführungseinheit relativ zueinander zumindest linearbeweglich verstellbar gelagert. Insbesondere ist die weitere Einstelleinheit dazu vorgesehen, die Formschenkel der Formführungseinheit entlang von unterschiedlichen, insbesondere quer zueinander verlaufenden, Verstellrichtungen linearbeweglich verstellbar zu lagern, insbesondere zu einer Gewährleistung von unterschiedlichen Produktbreiten. Vorzugsweise verlaufen die Verstellrichtungen in einer gemeinsamen, sich insbesondere zumindest im Wesentlichen parallel zu der Auflagefläche erstreckenden, Ebene und schließen insbesondere gleiche Winkel mit der Transportrichtung des Verpackungsmaterialschlauchs ein. Alternativ oder zusätzlich können die Formschenkel der Formführungseinheit relativ zueinander zumindest schwenkbeweglich, insbesondere in einer sich zumindest im Wesentlichen parallel zu der Auflagefläche erstreckenden Schwenkebene, verstellbar gelagert sein, insbesondere zu einer Einstellung der Breite des Verpackungsmaterialschlauchs. Insbesondere können die Formschenkel der Formführungseinheit an einem entlang der Transportrichtung des Verpackungsmaterialschlauchs von der Formeinheit abgewandten Endbereich der Formschenkel der Formführungseinheit schwenkbeweglich gelagert sein. Vorzugsweise kann der Endbereich der Formschenkel der Formführungseinheit separat von einem übrigen Bereich der Formführungseinheit, insbesondere entlang eines Trennschnitts von dem übrigen Bereich getrennt, ausgebildet, insbesondere montiert, sein. Insbesondere bildet jeweils ein Formschenkel der Formführungseinheit jeweils zumindest eine Formführungskontur der Formführungseinheit aus. Vorzugsweise sind die Formschenkel der Formführungseinheit um die gedachte Symmetrieebene spiegelsymmetrisch zueinander angeordnet, insbesondere gelagert. Vorteilhaft kann eine für unterschiedliche Produkte und/oder Verpackungsmaterialien optimierte Positionierung von Formschenkeln der Formeinheit und/oder der Formführungseinheit relativ zueinander ermöglicht werden.
- Ferner wird vorgeschlagen, dass die Formschenkel der Formführungseinheit einen in Transportrichtung des Verpackungsmaterialschlauchs V-förmig zulaufenden Führungsbereich ausbilden, der dazu vorgesehen ist, miteinander zu siegelnde Nahtbereiche des Verpackungsmaterialschlauchs zusammenzuführen. Insbesondere ist der Führungsbereich dazu vorgesehen, miteinander zu siegelnde Längssiegelnahtbereiche des Verpackungsmaterialschlauchs zusammenzuführen. Insbesondere weisen die Formschenkel der Formführungseinheit in einem der Formeinheit zugewandten Endbereich einen größeren Abstand entlang einer zumindest im Wesentlichen parallel zu der Auflagefläche und zumindest im Wesentlichen senkrecht zu der Transportrichtung des Verpackungsmaterialschlauchs verlaufenden Richtung zueinander auf als in dem der Formeinheit abgewandten Endbereich. Die Nahtbereiche des Verpackungsmaterialschlauchs sind insbesondere Bereiche, in denen das Verpackungsmaterial, insbesondere das Verpackungspapier, gesiegelt wird, insbesondere zur Erstellung einer Siegelnaht. Insbesondere ist der Führungsbereich dazu vorgesehen, die Nahtbereiche derart zusammenführen, dass die Nahtbereiche zu einer Siegelung aneinander anliegend zwischen jeweils zwei Siegelrollen der Paare von Siegelrollen hindurch transportierbar sind. Vorzugsweise mündet der Führungsbereich in dem der Formeinheit abgewandten Endbereich in eine von den Formschenkeln der Formführungseinheit gebildete Stützkontur, die dazu vorgesehen ist, den Verpackungsmaterialschlauch, insbesondere die zusammengeführten Nahtbereiche, zu stützen, insbesondere während eines Weitertransports bis zur Längssiegeleinheit. Vorteilhaft kann eine präzise Ausrichtung der Nahtbereiche zur Realisierung einer sauberen Siegelnaht, insbesondere Längssiegelnaht, ermöglicht werden.
- Weiterhin wird vorgeschlagen, dass die Horizontalformvorrichtung zumindest eine Heizeinheit umfasst, die dazu vorgesehen ist, die Formeinheit und/oder die Formführungseinheit zumindest abschnittsweise zu erhitzen, insbesondere zu einem Wärmeeintrag in einen, insbesondere in den vorgenannten, Nahtbereich. Insbesondere ist die Heizeinheit dazu vorgesehen, einen einer Siegelung, insbesondere einer Längssiegelung, des Verpackungsmaterials, insbesondere des Verpackungspapiers, vorgelagerten Wärmeeintrag in das Verpackungsmaterial, insbesondere in das Verpackungspapier, zu ermöglichen. Alternativ oder zusätzlich ist vorstellbar, dass die Heizeinheit dazu vorgesehen ist, das Verpackungsmaterial, insbesondere das Verpackungspapier, insbesondere an der Formführungseinheit, zu siegeln, insbesondere alternativ zu einer Siegelung durch die Längssiegeleinheit, und/oder einen erhöhten Wärmeeintrag zu gewährleisten, insbesondere in einem Bereich der Stützkontur der Formführungseinheit. Die Heizeinheit kann insbesondere als eine Heizwendel, als eine Heizpatrone, als eine Heizplatte, als ein Dickschichtheizelement oder als eine andere, einem Fachmann als sinnvoll erscheinende Heizeinheit ausgebildet sein. Vorzugsweise ist die Heizeinheit an der Formeinheit und/oder an der Formführungseinheit angeordnet, steht insbesondere in direktem Kontakt mit der Formeinheit und/oder der Formführungseinheit. Insbesondere kann die Horizontalformvorrichtung eine Mehrzahl von Heizeinheiten aufweisen, wobei jeweils zumindest eine Heizeinheit der Formeinheit und jeweils zumindest eine weitere Heizeinheit der Formführungseinheit zugeordnet sein kann. Insbesondere ist die Heizeinheit auf einer einer Kontaktfläche mit dem Verpackungsmaterial, insbesondere mit dem Verpackungspapier, abgewandten Seite der Formeinheit und/oder der Formführungseinheit angeordnet. Zusätzlich ist eine Heizung, die parallel zu einer Fläche der Formeinheit, insbesondere von der Formeinheit beabstandet, angeordnet ist, denkbar, welche das Verpackungsmaterial auf einer Innenseite beheizt.
- Insbesondere sind/ist die Formeinheit und/oder die Formführungseinheit dazu vorgesehen, von der Heizeinheit aufgenommene Wärmeenergie auf das Verpackungsmaterial, insbesondere auf das Verpackungspapier, zu übertragen. Insbesondere sind/ist die Formeinheit, insbesondere die Formschenkel der Formeinheit, und/oder die Formführungseinheit, insbesondere die Formschenkel der Formführungseinheit, aus einem wärmeleitfähigen Material, insbesondere aus einem Metall, ausgebildet. Insbesondere sind/ist die Formeinheit und/oder die Formführungseinheit an der Kontaktfläche mit dem Verpackungsmaterial, insbesondere mit dem Verpackungspapier, dazu vorgesehen, eine von der Heizeinheit bereitgestellte Wärmeenergie auf das Verpackungsmaterial, insbesondere in den Nahtbereichen, zu übertragen. Insbesondere ist durch einen Wärmeeintrag in die Nahtbereiche zumindest eine Siegelschicht des Verpackungspapiers aktivierbar. Vorteilhaft kann eine effiziente Siegelung des Verpackungsmaterials, insbesondere des Verpackungspapiers, ermöglicht werden.
- Zudem wird vorgeschlagen, dass die Horizontalformvorrichtung zumindest eine Luftdruckeinheit umfasst, die dazu vorgesehen ist, an der Formeinheit und/oder an der Formführungseinheit einen Unterdruck und/oder einen Überdruck auf ein Verpackungsmaterial auszuüben. Unter einem "Unterdruck" soll insbesondere ein Luftdruck verstanden werden, der geringer ist als ein Umgebungsluftdruck der Horizontalformvorrichtung. Unter einem "Überdruck" soll insbesondere ein Luftdruck verstanden werden, der höher ist als ein Umgebungsluftdruck der Horizontalformvorrichtung. Die Luftdruckeinheit kann insbesondere als ein Gebläse, als ein Sauger oder als eine andere, einem Fachmann als sinnvoll erscheinende Luftdruckeinheit ausgebildet sein. Insbesondere kann die Horizontalformvorrichtung eine Mehrzahl von Luftdruckeinheiten aufweisen, wobei jeweils zumindest eine Luftdruckeinheit der Formeinheit und jeweils zumindest eine weitere Luftdruckeinheit der Formführungseinheit zugeordnet sein kann. Insbesondere ist die Luftdruckeinheit auf der der Kontaktfläche mit dem Verpackungsmaterial, insbesondere mit dem Verpackungspapier, abgewandten Seite der Formeinheit und/oder der Formführungseinheit angeordnet. Bevorzugt sind/ist die Formeinheit, insbesondere die Formschenkel der Formeinheit, und/oder die Formführungseinheit, insbesondere die Formschenkel der Formführungseinheit, zumindest abschnittsweise perforiert, insbesondere aus einem porösen Material, ausgebildet. Insbesondere kann Luft einer von der Luftdruckeinheit erzeugten Luftströmung zumindest abschnittsweise durch die Formeinheit und/oder die Formführungseinheit strömen. Vorzugsweise ist die Luftdruckeinheit dazu vorgesehen, einen Unterdruck zu einer Ansaugung des Verpackungspapiers an die Formeinheit und/oder an die Formführungseinheit zu erzeugen, insbesondere zu einer Realisierung einer faltenarmen Anlage des Verpackungspapiers an der Formeinheit und/oder an der Formführungseinheit. Vorzugsweise ist die Luftdruckeinheit dazu vorgesehen, einen Überdruck zur Bildung eines Luftkissens an der Formeinheit und/oder an der Formführungseinheit zu erzeugen, insbesondere zu einer Realisierung eines reibungsarmen Transports des Verpackungspapiers entlang von der Formeinheit und/oder entlang von der Formführungseinheit. Bevorzugt ist die Luftdruckeinheit zwischen einer Erzeugung eines Unterdrucks und einer Erzeugung eines Überdrucks umschaltbar, insbesondere in Abhängigkeit von einer Anwendungssituation, beispielsweise in Abhängigkeit von einem verwendeten Verpackungsmaterial. Vorteilhaft kann ein besonders materialschonender Transport des Verpackungspapiers ermöglicht werden.
- Des Weiteren wird vorgeschlagen, dass die Horizontalformvorrichtung zumindest eine angetriebene Andruckeinheit, insbesondere eine Andruckrolle, umfasst, die dazu vorgesehen ist, ein Verpackungsmaterial mit einer Andruckkraft gegen die Formführungseinheit zu beaufschlagen. Vorzugsweise umfasst die Horizontalformvorrichtung die zumindest eine angetriebene Andruckeinheit alternativ oder zusätzlich zu einer der Formführungseinheit zugeordneten Luftdruckeinheit. Vorzugsweise umfasst die Horizontalformvorrichtung zumindest zwei angetriebene Andruckeinheiten, wobei jeweils zumindest eine angetriebene Andruckeinheit jeweils einem Formschenkel der Formführungseinheit zugeordnet ist, insbesondere dazu vorgesehen ist, das Verpackungsmaterial mit einer Andruckkraft gegen den Formschenkel zu beaufschlagen. Zusätzlich ist vorstellbar, dass die Horizontalformvorrichtung zumindest eine zusätzliche angetriebene Andruckeinheit, insbesondere eine zusätzliche Andruckrolle, umfasst, die dazu vorgesehen ist, das Verpackungsmaterial mit einer Andruckkraft gegen die Formeinheit zu beaufschlagen. Vorzugsweise sind die angetriebenen Andruckeinheiten als Andruckrollen ausgebildet, die zu Rotationsbewegungen antreibbar sind, insbesondere zu einem Transport des Verpackungsmaterialschlauchs entlang der Transportrichtung des Verpackungsmaterialschlauchs. Insbesondere sind die angetriebenen Andruckeinheiten dazu vorgesehen, den Verpackungsmaterialschlauch zwischen den angetriebenen Andruckeinheiten und der Formführungseinheit, insbesondere den Formschenkeln der Formführungseinheit, zu führen. Vorteilhaft kann eine besonders präzise Führung des Verpackungsmaterials ermöglicht werden.
- Ferner geht die Erfindung aus von einer Verpackungsmaschine, insbesondere von einer horizontalen Schlauchbeutelmaschine, mit zumindest einer erfindungsgemäßen Horizontalformvorrichtung. Vorzugsweise umfasst die Verpackungsmaschine zusätzlich zumindest die Verpackungsmaterialabwickeleinheit, die Verpackungsmaterialzuführeinheit, die Produktzuführeinheit, die Längssiegeleinheit und die Quersiegeleinheit. Vorteilhaft kann eine Verpackungsmaschine bereitgestellt werden, die eine besonders materialschonende Verpackung von Produkten ermöglicht.
- Die erfindungsgemäße Horizontalformvorrichtung und/oder die erfindungsgemä-ße Verpackungsmaschine sollen/soll hierbei nicht auf die oben beschriebene Anwendung und Ausführungsform beschränkt sein. Insbesondere können/kann die erfindungsgemäße Horizontalformvorrichtung und/oder die erfindungsgemäße Verpackungsmaschine zu einer Erfüllung einer hierin beschriebenen Funktionsweise eine von einer hierin genannten Anzahl von einzelnen Elementen, Bauteilen und Einheiten abweichende Anzahl aufweisen. Zudem sollen bei den in dieser Offenbarung angegebenen Wertebereichen auch innerhalb der genannten Grenzen liegende Werte als offenbart und als beliebig einsetzbar gelten.
- Weitere Vorteile ergeben sich aus der folgenden Zeichnungsbeschreibung. In den Zeichnungen sind vier Ausführungsbeispiele der Erfindung dargestellt. Die Zeichnungen, die Beschreibung und die Ansprüche enthalten zahlreiche Merkmale in Kombination. Der Fachmann wird die Merkmale zweckmäßigerweise auch einzeln betrachten und zu sinnvollen weiteren Kombinationen zusammenfassen.
- Es zeigen:
- Fig. 1
- einen Teil einer erfindungsgemäßen Verpackungsmaschine in einer schematischen Darstellung,
- Fig. 2
- einen Teil einer erfindungsgemäßen Horizontalformvorrichtung der erfindungsgemäßen Verpackungsmaschine aus
Fig. 1 in einer schematischen perspektivischen Darstellung, - Fig. 3
- einen Teil der erfindungsgemäßen Verpackungsmaschine aus
Fig. 1 in einer schematischen perspektivischen Darstellung, - Fig. 4
- einen Teil der erfindungsgemäßen Horizontalformvorrichtung der erfindungsgemäßen Verpackungsmaschine aus
Fig. 1 in einer weiteren schematischen perspektivischen Darstellung, - Fig. 5
- einen Teil einer ersten alternativen erfindungsgemäßen Horizontalformvorrichtung in einer schematischen perspektivischen Darstellung,
- Fig. 6
- einen Teil einer zweiten alternativen erfindungsgemäßen Horizontalformvorrichtung in einer schematischen perspektivischen Darstellung und
- Fig. 7
- einen Teil einer dritten alternativen erfindungsgemäßen Horizontalformvorrichtung in einer schematischen perspektivischen Darstellung.
-
Figur 1 zeigt einen Teil einer Verpackungsmaschine 50a in einer schematischen Darstellung. Bevorzugt umfasst die Verpackungsmaschine 50a eine Horizontalformvorrichtung 10a, insbesondere für horizontale Schlauchbeutelmaschinen, mit zumindest einer, insbesondere rollenfreien, Formeinheit 12a, insbesondere einer Formschulter, die dazu vorgesehen ist, eine Verpackungsmaterialbahn 14a, insbesondere eine Papierbahn und/oder eine Folienbahn, zu einem Verpackungsmaterialschlauch 16a zu formen. Die Verpackungsmaschine 50a ist insbesondere als eine horizontale Schlauchbeutelmaschine ausgebildet. Insbesondere ist die Horizontalformvorrichtung 10a dazu vorgesehen, ein Verpackungsmaterial 46a, insbesondere den Verpackungsmaterialschlauch 16a, entlang einer horizontalen, insbesondere entlang einer zumindest im Wesentlichen senkrecht zu einer Gravitationskraftwirkrichtung 52a verlaufenden, Transportrichtung 38a zu führen. - Vorzugsweise ist die Horizontalformvorrichtung 10a zumindest zu einer Formung und/oder Führung der Verpackungsmaterialbahn 14a vorgesehen, wobei das Verpackungsmaterial 46a bevorzugt als ein Papier und/oder als eine Folie ausgebildet ist. Insbesondere ist die Verpackungsmaterialbahn 14a als eine Papierbahn und/oder als eine Folienbahn ausgebildet. Vorzugsweise kann die Horizontalformvorrichtung 10a zusätzlich oder zumindest alternativ zu einer Formung und/oder Führung einer Verpackungsmaterialbahn 14a vorgesehen sein, wobei das Verpackungsmaterial 46a verschieden von einem Papier, beispielsweise als ein Kunststoff, ausgebildet ist. Insbesondere kann die Verpackungsmaterialbahn 14a alternativ aus einem Kunststoff ausgebildet sein. Das Verpackungsmaterial 46a ist insbesondere zu einer Verpackung, insbesondere zu einer Umhüllung, von Produkten 24a, insbesondere von Lebensmittelprodukten, vorgesehen (vgl.
Figur 3 ). Das Verpackungsmaterial 46a ist bevorzugt als ein Verpackungspapier ausgebildet. Vorzugsweise umfasst die Verpackungsmaschine 50a zumindest eine Verpackungsmaterialabwickeleinheit 54a, die dazu vorgesehen ist, das Verpackungsmaterial 46a, insbesondere als eine Verpackungsmaterialrolle 56a, aufzunehmen. Vorzugsweise ist die Verpackungsmaterialabwickeleinheit 54a dazu vorgesehen, das Verpackungsmaterial 46a als eine Verpackungsmaterialbahn 14a abzuwickeln, insbesondere einer Verpackungsmaterialzuführeinheit 58a der Verpackungsmaschine 50a zuzuführen. Die Verpackungsmaterialzuführeinheit 58a ist insbesondere dazu vorgesehen, der Horizontalformvorrichtung 10a, insbesondere der Formeinheit 12a, die Verpackungsmaterialbahn 14a zuzuführen. Die Verpackungsmaterialzuführeinheit 58a kann eine Mehrzahl von, insbesondere einem Fachmann bekannten, Komponenten, wie beispielsweise zumindest einen Schwinghebel, zumindest einen Zentriertaster, zumindest eine Bahnkantensteuerung und/oder zumindest eine Druckeinheit zu einem Bedrucken des Verpackungsmaterials 46a, umfassen. - Insbesondere ist der Verpackungsmaterialschlauch 16a dazu vorgesehen, zu verpackende Produkte 24a zu umhüllen. Insbesondere weist die Verpackungsmaschine 50a zumindest eine Produktzuführeinheit 60a, insbesondere ein Förderband, eine Mitnehmerkette o. dgl., auf, die dazu vorgesehen ist, die zu verpackenden Produkte 24a zu einer Umhüllung durch den Verpackungsmaterialschlauch 16a in einen Bereich der Horizontalformvorrichtung 10a, insbesondere der Formeinheit 12a, zu transportieren. Vorzugsweise verläuft eine Transportrichtung 62a der Produkte 24a zumindest im Wesentlichen parallel zu einer Transportrichtung 38a des Verpackungsmaterialschlauchs 16a.
- Vorzugsweise umfasst die Verpackungsmaschine 50a zumindest eine Längssiegeleinheit 64a, die dazu vorgesehen ist eine, insbesondere zumindest im Wesentlichen parallel zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a verlaufende, Längssiegelnaht des Verpackungsmaterialschlauchs 16a zu erstellen, insbesondere durch einen Druck auf das Verpackungsmaterial 46a und/oder durch einen Wärmeeintrag in das Verpackungsmaterial 46a. Die Längssiegeleinheit 64a ist entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a nach der Horizontalformvorrichtung 10a, insbesondere nach einer Formführungseinheit 18a der Horizontalformvorrichtung 10a (vgl. Figur 2), angeordnet. Insbesondere umfasst die Längssiegeleinheit 64a zumindest ein Paar von, insbesondere beheizbaren, profilierten und/oder mit Druck beaufschlagbaren, Siegelrollen 66a, 68a, die dazu vorgesehen sind, insbesondere durch eine Rotation, den Verpackungsmaterialschlauch 16a zu transportieren (vgl.
Figur 2 ). Vorzugsweise umfasst die Längssiegeleinheit 64a eine Mehrzahl von Paaren von Siegelrollen 66a, 68a, wobei zumindest ein erstes entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a nach der Horizontalformvorrichtung 10a angeordnetes Paar von Siegelrollen 66a beheizungsfrei, insbesondere zu einem beheizungsfreien Transport des Verpackungsmaterialschlauchs 16a, ausgebildet ist. Vorzugsweise umfasst die Verpackungsmaschine 50a zumindest eine Quersiegeleinheit 70a, die dazu vorgesehen ist, insbesondere nach jeweils einem Produkt 24a, Quersiegelnähte des Verpackungsmaterialschlauchs 16a, die insbesondere zumindest im Wesentlichen senkrecht zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a verlaufen, zu erstellen, insbesondere durch einen Druck auf das Verpackungsmaterial 46a und/oder durch einen Wärmeeintrag in das Verpackungsmaterial 46a. Insbesondere ist die Quersiegeleinheit 70a dazu vorgesehen, den Verpackungsmaterialschlauch 16a in einzelne Verpackungen, die insbesondere jeweils ein Produkt 24a umschließen, zu vereinzeln. Die Quersiegeleinheit 70a ist entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a nach der Längssiegeleinheit 64a angeordnet. Die Formeinheit 12a ist vorzugsweise dazu vorgesehen, die Verpackungsmaterialbahn 14a umzulenken. Insbesondere ist die Verpackungsmaterialzuführeinheit 58a dazu vorgesehen, der Formeinheit 12a die Verpackungsmaterialbahn 14a entlang einer quer, insbesondere zumindest im Wesentlichen senkrecht, zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a verlaufenden Richtung, insbesondere Einlaufrichtung 20a, zuzuführen. -
Figur 2 zeigt einen Teil der Horizontalformvorrichtung 10a der Verpackungsmaschine 50a ausFigur 1 in einer schematischen perspektivischen Darstellung. Bevorzugt umfasst die Horizontalformvorrichtung 10a zumindest eine, insbesondere die vorgenannte, Formführungseinheit 18a, insbesondere eine weitere Formschulter, die dazu vorgesehen ist, den Verpackungsmaterialschlauch 16a quer zu einer, insbesondere quer zu der vorgenannten, Einlaufrichtung 20a der Verpackungsmaterialbahn 14a an der Formeinheit 12a unter Erhalt einer von der Formeinheit 12a erzeugten, insbesondere homogenen, Materialspannung weiterzuführen. Die Formeinheit 12a weist vorzugsweise zumindest eine Faltkante 72a auf, um die die Verpackungsmaterialbahn 14a umlenkbar ist. Bevorzugt ist die Faltkante 72a als eine Schulterkante und die Formeinheit 12a als eine Formschulter ausgebildet. Insbesondere ist die Formeinheit 12a frei von Rollen zu einer Umlenkung der Verpackungsmaterialbahn 14a ausgebildet. Vorzugsweise ist die Formeinheit 12a dazu vorgesehen, die Verpackungsmaterialbahn 14a an der Faltkante 72a in eine Richtung quer zu der Einlaufrichtung 20a der Verpackungsmaterialbahn 14a und quer zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a umzulenken. Insbesondere erstreckt sich die Faltkante 72a zumindest im Wesentlichen senkrecht zu der Einlaufrichtung 20a der Verpackungsmaterialbahn 14a und zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a. Insbesondere sind/ist die Faltkante 72a und/oder zumindest eine weitere Faltkante 110a der Formeinheit 12a dazu vorgesehen, eine homogene Materialspannung in dem Verpackungsmaterial 46a zu erzeugen. - Die Formführungseinheit 18a ist bevorzugt dazu vorgesehen, den Verpackungsmaterialschlauch 16a zumindest im Wesentlichen senkrecht zu der Einlaufrichtung 20a der Verpackungsmaterialbahn 14a an der Formeinheit 12a, insbesondere entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a, unter Erhalt der von der Formeinheit 12a, insbesondere von der Faltkante 72a und/oder von der weiteren Faltkante 110a, erzeugten homogenen Materialspannung weiterzuführen. Insbesondere ist die Formführungseinheit 18a entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a nach der Formeinheit 12a und insbesondere vor der Längssiegeleinheit 64a angeordnet. Vorzugsweise ist die Formführungseinheit 18a frei von Rollen zu einer Umlenkung des Verpackungsmaterialschlauchs 16a, insbesondere als eine weitere Formschulter, ausgebildet. Insbesondere kann die Formführungseinheit 18a eine zu einer Geometrie der Formeinheit 12a zumindest im Wesentlichen analoge Geometrie aufweisen.
- Bevorzugt ist die Formführungseinheit 18a getrennt von der Formeinheit 12a ausgebildet, insbesondere angeordnet. Vorzugsweise ist die Formführungseinheit 18a als ein eigenständiges Bauteil oder als eine eigenständige Baugruppe, insbesondere aus zwei symmetrischen Bauteilen, ausgebildet. Insbesondere ist die Formführungseinheit 18a entlang einer zumindest im Wesentlichen senkrecht zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a verlaufenden Richtung, insbesondere entlang der Einlaufrichtung 20a der Verpackungsmaterialbahn 14a, und/oder, im vorliegenden Ausführungsbeispiel beispielhaft und, entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a beabstandet von der Formeinheit 12a angeordnet. Alternativ ist vorstellbar, dass die Formführungseinheit 18a einteilig mit der Formeinheit 12a, insbesondere als ein Formführungsfortsatz der Formeinheit 12a, ausgebildet ist.
- Bevorzugt umfasst die Horizontalformvorrichtung 10a zumindest eine Auflagefläche 22a, insbesondere eine Arbeitsplatte, auf der zu verpackende Produkte 24a transportierbar sind, wobei die Formeinheit 12a und die Formführungseinheit 18a auf voneinander abgewandten Seiten 26a, 28a der Auflagefläche 22a angeordnet sind. Die Auflagefläche 22a bildet vorzugsweise eine Stückbahn aus, auf der die Produkte 24a transportierbar sind. Die Auflagefläche 22a erstreckt sich vorzugsweise zumindest im Wesentlichen parallel zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a. Vorzugsweise sind/ist die Produktzuführeinheit 60a, die Längssiegeleinheit 64a, insbesondere die Siegelrollen 66a, 68a, und/oder die Quersiegeleinheit 70a zumindest abschnittsweise innerhalb der Auflagefläche 22a angeordnet, erstrecken/erstreckt sich zumindest abschnittsweise durch die Auflagefläche 22a hindurch. Insbesondere verlaufen Rotationsachsen 74a, 76a der Siegelrollen 66a, 68a der Längssiegeleinheit 64a zumindest im Wesentlichen senkrecht zu der Auflagefläche 22a. Vorzugsweise ist die Formeinheit 12a auf einer Seite 26a der Auflagefläche 22a angeordnet, auf der die Produkte 24a transportierbar sind und auf der insbesondere die Verpackungsmaterialabwickeleinheit 54a und die Verpackungsmaterialzuführeinheit 58a angeordnet sind. Die Formführungseinheit 18a ist vorzugsweise auf einer weiteren Seite 28a der Auflagefläche 22a angeordnet, auf der insbesondere die Längssiegeleinheit 64a zumindest zu einem Großteil, insbesondere mehr als 50 % einer maximalen Erstreckung der Längssiegeleinheit 64a zumindest im Wesentlichen parallel zu den Rotationsachsen 74a, 76a der Siegelrollen 66a, 68a, angeordnet ist. Insbesondere kann die Formführungseinheit 18a zumindest abschnittsweise mit der Auflagefläche 22a gekoppelt sein. Insbesondere erstreckt sich der Verpackungsmaterialschlauch 16a zumindest abschnittsweise durch die Auflagefläche 22a hindurch, insbesondere auf die weitere Seite 28a der Auflagefläche 22a.
-
Figur 3 zeigt einen Teil der Verpackungsmaschine 50a ausFigur 1 in einer schematischen perspektivischen Darstellung. Bevorzugt weist die Horizontalformvorrichtung 10a zumindest einen, insbesondere U-förmigen, Produkt- und/oder Verpackungsmaterialführungstunnel 78a auf, der dazu vorgesehen ist, den Verpackungsmaterialschlauch 16a zu stützen. Der Produkt- und/oder Verpackungsmaterialführungstunnel 78a ist insbesondere auf der der Formeinheit 12a zugewandten Seite 26a der Auflagefläche 22a angeordnet, insbesondere an der Auflagefläche 22a befestigt. Der Produkt- und/oder Verpackungsmaterialführungstunnel 78a erstreckt sich insbesondere entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a von zumindest vor der Formeinheit 12a bis zur Formeinheit 12a, bevorzugt bis zur Formführungseinheit 18a und besonders bevorzugt bis zu dem ersten Paar von Siegelrollen 66a der Längssiegeleinheit 64a. Vorzugsweise weist der Produkt- und/oder Verpackungsmaterialführungstunnel 78a einen zumindest im Wesentlichen analog zu einem Querschnitt von zu verpackenden Produkten 24a ausgebildeten Querschnitt, insbesondere einen leicht größeren Querschnitt als die zu verpackenden Produkte 24a, auf. Insbesondere sind die Produkte 24a innerhalb des Produkt- und/oder Verpackungsmaterialführungstunnels 78a transportierbar. Vorzugsweise ist die Formeinheit 12a dazu vorgesehen, den Verpackungsmaterialschlauch 16a zumindest abschnittsweise um den Produkt- und/oder Verpackungsmaterialführungstunnel 78a, insbesondere um Außenkanten des Produkt- und/oder Verpackungsmaterialführungstunnels 78a, zu formen. Insbesondere ist der Produkt- und/oder Verpackungsmaterialführungstunnel 78a dazu vorgesehen, den Verpackungsmaterialschlauch 16a, insbesondere zusätzlich zu der Formführungseinheit 18a, zu stützen. Alternativ ist denkbar, dass die Horizontalformvorrichtung 10a und die Verpackungsmaschine 50a frei von dem Produkt- und/oder Verpackungsmaterialführungstunnel 78a ausgebildet sind. -
Figur 4 zeigt einen Teil der Horizontalformvorrichtung 10a der Verpackungsmaschine 50a ausFigur 1 in einer weiteren schematischen perspektivischen Darstellung. Die Formeinheit 12a weist vorzugsweise zumindest zwei Formkonturkanten 80a, die sich ausgehend von der Faltkante 72a quer zu der Faltkante 72a, insbesondere V-förmig, erstrecken, auf. Insbesondere ist die Verpackungsmaterialbahn 14a um die Formkonturkanten 80a und um die weitere Faltkante 110a zu dem Verpackungsmaterialschlauch 16a umformbar. Vorzugsweise erstrecken sich die Formkonturkanten 80a entlang einer Laufrichtung des Verpackungsmaterials 46a und/oder entlang einer Außenkontur der zugeführten Produkte 24a von der Faltkante 72a bis zur weiteren Faltkante 110a, insbesondere bis zu einem Formtunnel 82a der Formeinheit 12a, der dazu vorgesehen ist, den Verpackungsmaterialschlauch 16a entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a zu führen. Insbesondere verläuft eine Längsachse 84a des Formtunnels 82a zumindest im Wesentlichen parallel zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a. Vorzugsweise umfasst die Formführungseinheit 18a zumindest eine, insbesondere dreidimensionale, Formführungskontur 86a, die dazu vorgesehen ist, den geführten Verpackungsmaterialschlauch 16a, insbesondere zumindest eine Außenkante des Verpackungsmaterialschlauchs 16a, zu stützen, insbesondere zu einer Realisierung einer Aufrechterhaltung der homogenen Materialspannung. Vorzugsweise weist die Formführungseinheit 18a zumindest zwei Formführungskonturen 86a auf, die insbesondere spiegelsymmetrisch um eine gedachte Symmetrieebene, die sich zumindest im Wesentlichen parallel zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a erstreckt, in der insbesondere die Transportrichtung 38a des Verpackungsmaterialschlauchs 16a verläuft, und die sich zumindest im Wesentlichen senkrecht zu der Faltkante 72a der Formeinheit 12a erstreckt, angeordnet sind. Vorzugsweise ist die Formführungseinheit 18a, insbesondere um die gedachte Symmetrieebene, spiegelsymmetrisch ausgebildet. - Alternativ ist vorstellbar, dass die Formführungseinheit 18a und/oder die Formeinheit 12a asymmetrisch ausgebildet sind/ist.
- Bevorzugt umfasst die Horizontalformvorrichtung 10a zumindest eine Einstelleinheit 30a, 32a, die dazu vorgesehen ist, die Formeinheit 12a und die Formführungseinheit 18a zu einer Realisierung von unterschiedlichen Verpackungsmaterialschlauchgeometrien verstellbar zu lagern, insbesondere in unterschiedlichen Verstellebenen. Vorzugsweise umfasst die Horizontalformvorrichtung 10a zumindest zwei Einstelleinheiten 30a, 32a, wobei eine Einstelleinheit 30a dazu vorgesehen ist, die Formeinheit 12a verstellbar zu lagern, und wobei eine weitere Einstelleinheit 32a dazu vorgesehen ist, die Formführungseinheit 18a verstellbar zu lagern. Insbesondere können zu einer Verpackung von unterschiedlichen Produkten 24a unterschiedliche Verpackungsmaterialschlauchgeometrien benötigt werden. Insbesondere ist die Verpackungsmaschine 50a zu einer Verpackung von unterschiedlichen Produkten 24a, die insbesondere unterschiedliche Abmessungen aufweisen, vorgesehen. Insbesondere können unterschiedliche Verpackungsmaterialschlauchgeometrien zur Verpackung von unterschiedlichen Produkten 24a, die unterschiedliche maximale Erstreckungen zumindest im Wesentlichen senkrecht zu der Auflagefläche 22a, insbesondere unterschiedliche Höhen, und/oder die unterschiedliche maximale Erstreckungen zumindest im Wesentlichen parallel zu der Auflagefläche 22a und zumindest im Wesentlichen senkrecht zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a, insbesondere unterschiedliche Breiten, aufweisen, benötigt werden. Insbesondere sind/ist durch eine Verstellung der Formeinheit 12a und/oder der Formführungseinheit 18a eine maximale Erstreckung des Verpackungsmaterialschlauchs 16a zumindest im Wesentlichen senkrecht zu der Auflagefläche 22a, insbesondere eine Höhe des Verpackungsmaterialschlauchs 16a, und/oder eine maximale Erstreckung des Verpackungsmaterialschlauchs 16a zumindest im Wesentlichen parallel zu der Auflagefläche 22a und zumindest im Wesentlichen senkrecht zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a, insbesondere eine Breite des Verpackungsmaterialschlauchs 16a, einstellbar. Insbesondere kann die Formführungseinheit 18a mittels der weiteren Einstelleinheit 32a zu einer Korrektur ungleichmäßiger Spannungsverhältnisse in dem Verpackungsmaterial 46a einstellbar sein.
- Vorzugsweise ist die Formeinheit 12a in zumindest einer sich auf der der Formeinheit 12a zugewandten Seite 26a der Auflagefläche 22a erstreckenden Verstellebene verstellbar gelagert. Vorzugsweise ist die Formführungseinheit 18a in zumindest einer weiteren, sich auf der weiteren, der Formführungseinheit 18a zugewandten Seite 28a der Auflagefläche 22a erstreckenden Verstellebene verstellbar gelagert. Insbesondere sind/ist die Formeinheit 12a und/oder die Formführungseinheit 18a als ganzes Bauteil oder als ganze Baugruppe verstellbar gelagert. Insbesondere sind/ist die Formeinheit 12a und/oder die Formführungseinheit 18a in sich selbst verstellbar, insbesondere einzelne Komponenten der Formeinheit 12a relativ zueinander und/oder einzelne Komponenten der Formführungseinheit 18a relativ zueinander.
- Bevorzugt ist/sind die zumindest eine Einstelleinheit 30a, 32a, insbesondere die Einstelleinheiten 30a, 32a, dazu vorgesehen, die Formeinheit 12a und die Formführungseinheit 18a relativ zueinander verstellbar zu lagern. Insbesondere sind die Einstelleinheiten 30a, 32a dazu vorgesehen, die Formeinheit 12a und die Formführungseinheit 18a als ganzes Bauteil oder als ganze Baugruppe relativ zueinander verstellbar zu lagern. Vorzugsweise sind die Einstelleinheiten 30a, 32a dazu vorgesehen, die Formeinheit 12a und die Formführungseinheit 18a linearbeweglich und/oder schwenkbeweglich zu lagern. Vorzugsweise ist die Einstelleinheit 30a dazu vorgesehen, die Formeinheit 12a, insbesondere zu einer Einstellung einer Höhe des Verpackungsmaterialschlauchs 16a, zumindest linearbeweglich entlang einer zumindest im Wesentlichen senkrecht zu der Auflagefläche 22a verlaufenden Verstellrichtung 88a zu lagern. Insbesondere umfasst die Einstelleinheit 30a zumindest eine Linearführung 90a, die dazu vorgesehen ist, die Formeinheit 12a linearbeweglich entlang der Verstellrichtung 88a zu lagern. Insbesondere umfasst die Einstelleinheit 30a zumindest eine weitere Linearführung 112a, die dazu vorgesehen ist, die Formeinheit 12a linearbeweglich entlang einer zumindest im Wesentlichen senkrecht zu der Verstellrichtung 88a und zumindest im Wesentlichen parallel zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a verlaufenden weiteren Verstellrichtung 114a zu lagern (vgl.
Figur 3 ). Vorzugsweise ist die weitere Einstelleinheit 32a dazu vorgesehen, die Formführungseinheit 18a zumindest linearbeweglich entlang zumindest einer zumindest im Wesentlichen parallel zu der Auflagefläche 22a, insbesondere quer zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a, verlaufenden Verstellrichtung 92a, 116a zu lagern. Vorzugsweise sind die Einstelleinheiten 30a, 32a als manuelle Einstelleinheiten zu einer manuellen Verstellung der Formeinheit 12a und der Formführungseinheit 18a, insbesondere relativ zueinander, ausgebildet. Alternativ oder zusätzlich ist vorstellbar, dass zumindest eine der Einstelleinheiten 30a, 32a zumindest ein automatisches Verstellelement, insbesondere einen Stellmotor, aufweist, das/der zu einer automatischen Verstellung der Formeinheit 12a und/oder der Formführungseinheit 18a vorgesehen ist. - Bevorzugt ist/sind die zumindest eine Einstelleinheit 30a, 32a, insbesondere die Einstelleinheiten 30a, 32a, dazu vorgesehen, zumindest zwei Formschenkel 34a, 36a der Formeinheit 12a und/oder der Formführungseinheit 18a relativ zueinander verstellbar zu lagern. Vorzugsweise weist die Formeinheit 12a zumindest zwei Formschenkel 34a auf, die relativ zueinander verstellbar, insbesondere linearbeweglich und/oder schwenkbeweglich, gelagert sind. Insbesondere sind die Formschenkel 34a der Formeinheit 12a relativ zueinander zumindest linearbeweglich, insbesondere entlang einer zumindest im Wesentlichen parallel zu der Faltkante 72a, insbesondere zu einer Faltkantenlauffläche, verlaufenden Richtung, verstellbar gelagert. Insbesondere umfasst die Einstelleinheit 30a zumindest ein Querlagerelement 94a, das dazu vorgesehen ist, die Formschenkel 34a der Formeinheit 12a relativ zueinander zumindest linearbeweglich zu lagern. Insbesondere bilden die Formschenkel 34a der Formeinheit 12a die Faltkante 72a, insbesondere die Faltkantenlauffläche, gemeinsam aus. Insbesondere sind die Formschenkel 34a der Formeinheit 12a, insbesondere entlang der zumindest im Wesentlichen parallel zu der Faltkante 72a verlaufenden Richtung, aufeinander zu und voneinander weg beweglich gelagert, insbesondere zu einer Einstellung einer Breite des Verpackungsmaterialschlauchs 16a. Insbesondere bilden die Formschenkel 34a der Formeinheit 12a gemeinsam den Formtunnel 82a der Formeinheit 12a aus. Insbesondere bildet jeweils ein Formschenkel 34a der Formeinheit 12a jeweils zumindest eine Formkonturkante 80a der Formeinheit 12a aus. Die Einstelleinheit 30a weist vorzugsweise zumindest ein Zwischenelement 96a, insbesondere eine Mehrzahl von Zwischenelementen 96a, zu einer Ausfüllung eines Raums zwischen den zwei voneinander wegbewegten Formschenkeln 34a der Formeinheit 12a auf, insbesondere zu einer Gewährleistung von unterschiedlichen Produktbreiten.
- Vorzugsweise weist die Formführungseinheit 18a zumindest zwei Formschenkel 36a auf, die relativ zueinander verstellbar, insbesondere linearbeweglich und/oder schwenkbeweglich, gelagert sind. Insbesondere kann die weitere Einstelleinheit 32a, die zu einer verstellbaren Lagerung der Formführungseinheit 18a vorgesehen ist, in einer alternativen Ausgestaltungsform zumindest im Wesentlichen analog zu der Einstelleinheit 30a, die zu einer verstellbaren Lagerung der Formeinheit 12a vorgesehen ist, ausgebildet sein. Vorzugsweise sind die Formschenkel 36a der Formführungseinheit 18a relativ zueinander zumindest linearbeweglich verstellbar gelagert. Insbesondere ist die weitere Einstelleinheit 32a dazu vorgesehen, die Formschenkel 36a der Formführungseinheit 18a entlang von unterschiedlichen, insbesondere quer zueinander verlaufenden, Verstellrichtungen 92a, 116a linearbeweglich verstellbar zu lagern, insbesondere zu einer Gewährleistung von unterschiedlichen Produktbreiten. Vorzugsweise verlaufen die Verstellrichtungen 92a, 116a in einer gemeinsamen, sich insbesondere zumindest im Wesentlichen parallel zu der Auflagefläche 22a erstreckenden, Ebene und schließen insbesondere gleiche Winkel mit der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a ein. Alternativ oder zusätzlich können die Formschenkel 36a der Formführungseinheit 18a relativ zueinander zumindest schwenkbeweglich, insbesondere in einer sich zumindest im Wesentlichen parallel zu der Auflagefläche 22a erstreckenden Schwenkebene, verstellbar gelagert sein, insbesondere zu einer Einstellung der Breite des Verpackungsmaterialschlauchs 16a. Insbesondere können die Formschenkel 36a der Formführungseinheit 18a in einer alternativen Ausführungsform an einem entlang der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a von der Formeinheit 12a abgewandten Endbereich 98a der Formschenkel 36a der Formführungseinheit 18a schwenkbeweglich gelagert sein. Vorzugsweise kann der Endbereich 98a der Formschenkel 36a der Formführungseinheit 18a in einer alternativen Ausführungsform separat von einem übrigen Bereich der Formführungseinheit 18a, insbesondere entlang eines Trennschnitts 118a von dem übrigen Bereich getrennt, ausgebildet, insbesondere montiert, sein. Insbesondere bildet jeweils ein Formschenkel 36a der Formführungseinheit 18a jeweils zumindest eine Formführungskontur 86a der Formführungseinheit 18a aus. Vorzugsweise sind die Formschenkel 36a der Formführungseinheit 18a um die gedachte Symmetrieebene spiegelsymmetrisch zueinander angeordnet, insbesondere gelagert.
- Bevorzugt bilden die Formschenkel 36a der Formführungseinheit 18a einen in Transportrichtung 38a des Verpackungsmaterialschlauchs 16a V-förmig zulaufenden Führungsbereich 40a aus, der dazu vorgesehen ist, miteinander zu siegelnde Nahtbereiche des Verpackungsmaterialschlauchs 16a zusammenzuführen. Insbesondere ist der Führungsbereich 40a dazu vorgesehen, miteinander zu siegelnde Längssiegelnahtbereiche des Verpackungsmaterialschlauchs 16a zusammenzuführen. Insbesondere weisen die Formschenkel 36a der Formführungseinheit 18a in einem der Formeinheit 12a zugewandten Endbereich 100a einen größeren Abstand entlang einer zumindest im Wesentlichen parallel zu der Auflagefläche 22a und zumindest im Wesentlichen senkrecht zu der Transportrichtung 38a des Verpackungsmaterialschlauchs 16a verlaufenden Richtung zueinander auf als in dem der Formeinheit 12a abgewandten Endbereich 98a. Die Nahtbereiche des Verpackungsmaterialschlauchs 16a sind insbesondere Bereiche, in denen das Verpackungsmaterial 46a, insbesondere das Verpackungspapier, gesiegelt wird, insbesondere zur Erstellung einer Siegelnaht. Insbesondere ist der Führungsbereich 40a dazu vorgesehen, die Nahtbereiche derart zusammenführen, dass die Nahtbereiche zu einer Siegelung aneinander anliegend zwischen jeweils zwei Siegelrollen 66a, 68a der Paare von Siegelrollen 66a, 68a hindurch transportierbar sind. Vorzugsweise mündet der Führungsbereich 40a in dem der Formeinheit 12a abgewandten Endbereich 98a in eine von den Formschenkeln 36a der Formführungseinheit 18a gebildete Stützkontur 102a, die dazu vorgesehen ist, den Verpackungsmaterialschlauch 16a, insbesondere die zusammengeführten Nahtbereiche, zu stützen, insbesondere während eines Weitertransports bis zur Längssiegeleinheit 64a.
- In den
Figuren 5 bis 7 sind drei weitere Ausführungsbeispiele der Erfindung gezeigt. Die nachfolgenden Beschreibungen und die Zeichnungen beschränken sich im Wesentlichen auf die Unterschiede zwischen den Ausführungsbeispielen, wobei bezüglich gleich bezeichneter Bauteile, insbesondere in Bezug auf Bauteile mit gleichen Bezugszeichen, grundsätzlich auch auf die Zeichnungen und/oder die Beschreibung der anderen Ausführungsbeispiele, insbesondere derFiguren 1 bis 4 , verwiesen werden kann. Zur Unterscheidung der Ausführungsbeispiele ist der Buchstabe a den Bezugszeichen des Ausführungsbeispiels in denFiguren 1 bis 4 nachgestellt. In den Ausführungsbeispielen derFiguren 5 bis 7 ist der Buchstabe a durch die Buchstaben b bis d ersetzt. -
Figur 5 zeigt einen Teil einer ersten alternativen Horizontalformvorrichtung 10b in einer schematischen perspektivischen Darstellung. Die Horizontalformvorrichtung 10b umfasst insbesondere zumindest eine Formeinheit 12b und zumindest eine Formführungseinheit 18b. Bevorzugt umfasst die Horizontalformvorrichtung 10b zumindest eine Heizeinheit 42b, die dazu vorgesehen ist, die Formeinheit 12b und/oder die Formführungseinheit 18b zumindest abschnittsweise zu erhitzen, insbesondere zu einem Wärmeeintrag in einen Nahtbereich, insbesondere eines Verpackungsmaterials. Insbesondere ist die Heizeinheit 42b dazu vorgesehen, einen einer Siegelung, insbesondere einer Längssiegelung, des Verpackungsmaterials, insbesondere eines Verpackungspapiers, einen vorgelagerten Wärmeeintrag in das Verpackungsmaterial, insbesondere in das Verpackungspapier, zu ermöglichen. Alternativ oder zusätzlich ist vorstellbar, dass die Heizeinheit 42b dazu vorgesehen ist, das Verpackungsmaterial, insbesondere das Verpackungspapier, insbesondere an der Formführungseinheit 18b, zu siegeln, insbesondere alternativ zu einer Siegelung durch eine Längssiegeleinheit einer Verpackungsmaschine, und/oder einen erhöhten Wärmeeintrag zu gewährleisten, insbesondere in einem Bereich einer Stützkontur 102b der Formführungseinheit 18b. Die Heizeinheit 42b kann insbesondere als eine Heizwendel, als eine Heizpatrone, als eine Heizplatte, als ein Dickschichtheizelement oder als eine andere, einem Fachmann als sinnvoll erscheinende Heizeinheit ausgebildet sein. Vorzugsweise ist die Heizeinheit 42b an der Formeinheit 12b und/oder an der Formführungseinheit 18b angeordnet, steht insbesondere in direktem Kontakt mit der Formeinheit 12b und/oder der Formführungseinheit 18b. Insbesondere kann die Horizontalformvorrichtung 10b eine Mehrzahl von Heizeinheiten 42b aufweisen, wobei jeweils zumindest eine Heizeinheit 42b der Formeinheit 12b und jeweils zumindest eine weitere Heizeinheit 42b der Formführungseinheit 18b zugeordnet sein kann. Insbesondere ist die Heizeinheit 42b auf einer einer Kontaktfläche 104b mit dem Verpackungsmaterial, insbesondere mit dem Verpackungspapier, abgewandten Seite der Formeinheit 12b und/oder der Formführungseinheit 18b angeordnet. Im vorliegenden Ausführungsbeispiel weist die Horizontalformvorrichtung 10b beispielhaft eine einzelne Heizeinheit 42b auf, die an der Formeinheit 12b, insbesondere auf der der Kontaktfläche 104b mit dem Verpackungsmaterial abgewandten Seite der Formeinheit 12b, angeordnet ist, insbesondere in direktem Kontakt mit der Formeinheit 12b steht. Zusätzlich ist eine Heizung, die parallel zu einer Fläche 120b der Formeinheit 12b, insbesondere von der Formeinheit 12b beabstandet, angeordnet ist, denkbar, welche das Verpackungsmaterial auf einer Innenseite beheizt. - Insbesondere sind/ist die Formeinheit 12b und/oder die Formführungseinheit 18b, im vorliegenden Ausführungsbeispiel beispielhaft die Formeinheit 12b, dazu vorgesehen, von der Heizeinheit 42b aufgenommene Wärmeenergie auf das Verpackungsmaterial, insbesondere auf das Verpackungspapier, zu übertragen. Insbesondere sind/ist die Formeinheit 12b, insbesondere die Formschenkel 34b der Formeinheit 12b, und/oder die Formführungseinheit 18b, insbesondere die Formschenkel 36b der Formführungseinheit 18b, im vorliegenden Ausführungsbeispiel beispielhaft zumindest die Formeinheit 12b, aus einem wärmeleitfähigen Material, insbesondere aus einem Metall, ausgebildet. Insbesondere sind/ist die Formeinheit 12b und/oder die Formführungseinheit 18b, im vorliegenden Ausführungsbeispiel beispielhaft die Formeinheit 12b, an der Kontaktfläche 104b mit dem Verpackungsmaterial, insbesondere mit dem Verpackungspapier, dazu vorgesehen, eine von der Heizeinheit 42b bereitgestellte Wärmeenergie auf das Verpackungsmaterial, insbesondere in den Nahtbereichen, zu übertragen. Insbesondere ist durch einen Wärmeeintrag in die Nahtbereiche zumindest eine Siegelschicht des Verpackungspapiers aktivierbar.
-
Figur 6 zeigt einen Teil einer zweiten alternativen Horizontalformvorrichtung 10c in einer schematischen perspektivischen Darstellung. Die Horizontalformvorrichtung 10c umfasst insbesondere zumindest eine Formeinheit 12c und zumindest eine Formführungseinheit 18c. Bevorzugt umfasst die Horizontalformvorrichtung 10c zumindest eine Luftdruckeinheit 44c, die dazu vorgesehen ist, an der Formeinheit 12c und/oder an der Formführungseinheit 18c einen Unterdruck und/oder einen Überdruck auf ein Verpackungsmaterial auszuüben. Im vorliegenden Ausführungsbeispiel weist die Horizontalformvorrichtung 10c beispielhaft zwei Luftdruckeinheiten 44c auf, wobei jeweils eine der Luftdruckeinheiten 44c dazu vorgesehen ist, an jeweils einem Formschenkel 36c der Formführungseinheit 18c einen Unterdruck und/oder einen Überdruck auf das Verpackungsmaterial auszuüben. Die Luftdruckeinheiten 44c können insbesondere als Gebläse, als Sauger oder als andere, einem Fachmann als sinnvoll erscheinende Luftdruckeinheiten ausgebildet sein. Insbesondere kann die Horizontalformvorrichtung 10c in einer alternativen Ausgestaltungsform eine Mehrzahl von Luftdruckeinheiten 44c aufweisen, wobei jeweils zumindest eine Luftdruckeinheit 44c der Formeinheit 12c und jeweils zumindest eine weitere Luftdruckeinheit 44c der Formführungseinheit 18c zugeordnet sein kann. Insbesondere sind die Luftdruckeinheiten 44c auf einer einer Kontaktfläche 106c mit dem Verpackungsmaterial, insbesondere mit einem Verpackungspapier, abgewandten Seite der Formeinheit 12c und/oder der Formführungseinheit 18c, im vorliegenden Ausführungsbeispiel beispielhaft der Formführungseinheit 18c, angeordnet. Bevorzugt sind/ist die Formeinheit 12c, insbesondere Formschenkel 34c der Formeinheit 12c, und/oder die Formführungseinheit 18c, insbesondere die Formschenkel 36c der Formführungseinheit 18c, im vorliegenden Ausführungsbeispiel beispielhaft die Formführungseinheit 18c, zumindest abschnittsweise perforiert, insbesondere aus einem porösen Material, ausgebildet. Insbesondere weisen die Formschenkel 36c der Formführungseinheit 18c eine Perforierung 108c auf. Insbesondere kann Luft einer von den Luftdruckeinheiten 44c erzeugten Luftströmung zumindest abschnittsweise durch die Formeinheit 12c und/oder die Formführungseinheit 18c, im vorliegenden Ausführungsbeispiel beispielhaft durch die Formführungseinheit 18c, strömen. Vorzugsweise sind die Luftdruckeinheiten 44c dazu vorgesehen, einen Unterdruck zu einer Ansaugung des Verpackungspapiers an die Formeinheit 12c und/oder an die Formführungseinheit 18c, im vorliegenden Ausführungsbeispiel beispielhaft an die Formführungseinheit 18c, zu erzeugen, insbesondere zu einer Realisierung einer faltenarmen Anlage des Verpackungspapiers an der Formeinheit 12c und/oder an der Formführungseinheit 18c, im vorliegenden Ausführungsbeispiel beispielhaft an der Formführungseinheit 18c. Vorzugsweise sind die Luftdruckeinheiten 44c dazu vorgesehen, einen Überdruck zur Bildung eines Luftkissens an der Formeinheit 12c und/oder an der Formführungseinheit 18c, im vorliegenden Ausführungsbeispiel beispielhaft an der Formführungseinheit 18c, zu erzeugen, insbesondere zu einer Realisierung eines reibungsarmen Transports des Verpackungspapiers entlang von der Formeinheit 12c und/oder entlang von der Formführungseinheit 18c, im vorliegenden Ausführungsbeispiel beispielhaft entlang von der Formführungseinheit 18c. Bevorzugt sind die Luftdruckeinheiten 44c zwischen einer Erzeugung eines Unterdrucks und einer Erzeugung eines Überdrucks umschaltbar, insbesondere in Abhängigkeit von einer Anwendungssituation, beispielsweise in Abhängigkeit von einem verwendeten Verpackungsmaterial. -
Figur 7 zeigt einen Teil einer dritten alternativen Horizontalformvorrichtung 10d in einer schematischen perspektivischen Darstellung. Die Horizontalformvorrichtung 10d umfasst zumindest eine Formeinheit 12d und zumindest eine Formführungseinheit 18d. Bevorzugt umfasst die Horizontalformvorrichtung 10d zumindest eine angetriebene Andruckeinheit 48d, insbesondere eine Andruckrolle, die dazu vorgesehen ist, ein Verpackungsmaterial mit einer Andruckkraft gegen die Formführungseinheit 18d zu beaufschlagen. Vorzugsweise umfasst die Horizontalformvorrichtung 10d die zumindest eine angetriebene Andruckeinheit 48d alternativ oder zusätzlich, im vorliegenden Ausführungsbeispiel beispielhaft alternativ, zu einer der Formführungseinheit 18d zugeordneten Luftdruckeinheit. Vorzugsweise umfasst die Horizontalformvorrichtung 10d zumindest zwei angetriebene Andruckeinheiten 48d, wobei jeweils zumindest eine angetriebene Andruckeinheit 48d jeweils einem Formschenkel 36d der Formführungseinheit 18d zugeordnet ist, insbesondere dazu vorgesehen ist, das Verpackungsmaterial mit einer Andruckkraft gegen den Formschenkel 36d zu beaufschlagen. Zusätzlich ist vorstellbar, dass die Horizontalformvorrichtung 10d zumindest eine zusätzliche angetriebene Andruckeinheit 48d, insbesondere eine zusätzliche Andruckrolle, umfasst, die dazu vorgesehen ist, das Verpackungsmaterial mit einer Andruckkraft gegen die Formeinheit 12d zu beaufschlagen. Vorzugsweise sind die angetriebenen Andruckeinheiten 48d als Andruckrollen ausgebildet, die zu Rotationsbewegungen antreibbar sind, insbesondere zu einem Transport eines Verpackungsmaterialschlauchs entlang einer Transportrichtung 38d des Verpackungsmaterialschlauchs. Insbesondere sind die angetriebenen Andruckeinheiten 48d dazu vorgesehen, den Verpackungsmaterialschlauch zwischen den angetriebenen Andruckeinheiten 48d und der Formführungseinheit 18d, insbesondere den Formschenkeln 36d der Formführungseinheit 18d, zu führen.
Claims (13)
- Horizontalformvorrichtung, insbesondere für horizontale Schlauchbeutelmaschinen, mit zumindest einer, insbesondere rollenfreien, Formeinheit (12a-12d), insbesondere einer Formschulter, die dazu vorgesehen ist, eine Verpackungsmaterialbahn (14a), insbesondere eine Papierbahn, zu einem Verpackungsmaterialschlauch (16a) zu formen, wobei die Formeinheit (12a-12d) zumindest eine Faltkante (72a-72d) aufweist, um die die Verpackungsmaterialbahn (14a) umlenkbar ist, und mit zumindest einer Formführungseinheit (18a-18d), insbesondere einer weiteren Formschulter, die dazu vorgesehen ist, den Verpackungsmaterialschlauch (16a) quer zu einer Einlaufrichtung (20a-20d) der Verpackungsmaterialbahn (14a) an der Formeinheit (12a-12d) unter Erhalt einer von der Formeinheit (12a-12d) erzeugten, insbesondere homogenen, Materialspannung weiterzuführen, gekennzeichnet durch zumindest eine Auflagefläche (22a), insbesondere eine Arbeitsplatte, auf der zu verpackende Produkte (24a) transportierbar sind, wobei die Formeinheit (12a-12d) und die Formführungseinheit (18a-18d) auf voneinander abgewandten Seiten (26a-26d, 28a-28d) der Auflagefläche (22a) angeordnet sind, wobei die Formführungseinheit (18a-18d) zumindest eine Formführungskontur (86a-86d) umfasst, die dazu vorgesehen ist, den geführten Verpackungsmaterialschlauch (16a) zu einer Realisierung einer Aufrechterhaltung der homogenen Materialspannung zu stützen.
- Horizontalformvorrichtung nach Anspruch 1, dadurch gekennzeichnet, dass die Formführungseinheit (18a-18d) getrennt von der Formeinheit (12a-12d) ausgebildet, insbesondere angeordnet, ist.
- Horizontalformvorrichtung nach einem der vorhergehenden Ansprüche, gekennzeichnet durch zumindest einen, insbesondere U-förmigen, Produkt- und/oder Verpackungsmaterialführungstunnel (78a), der dazu vorgesehen ist, den Verpackungsmaterialschlauch (16a) zu stützen.
- Horizontalformvorrichtung nach einem der vorhergehenden Ansprüche, gekennzeichnet durch zumindest eine Einstelleinheit (30a-30d, 32a-32d), die dazu vorgesehen ist, die Formeinheit (12a-12d) und die Formführungseinheit (18a-18d) zu einer Realisierung von unterschiedlichen Verpackungsmaterialschlauchgeometrien verstellbar zu lagern, insbesondere in unterschiedlichen Verstellebenen.
- Horizontalformvorrichtung nach Anspruch 4, dadurch gekennzeichnet, dass die zumindest eine Einstelleinheit (30a-30d, 32a-32d) dazu vorgesehen ist, die Formeinheit (12a-12d) und die Formführungseinheit (18a-18d) relativ zueinander verstellbar zu lagern.
- Horizontalformvorrichtung nach Anspruch 4 oder 5, dadurch gekennzeichnet, dass die zumindest eine Einstelleinheit (30a-30d, 32a-32d) dazu vorgesehen ist, zumindest zwei Formschenkel (34a-34d, 36a-36d) der Formeinheit (12a-12d) und/oder der Formführungseinheit (18a-18d) relativ zueinander verstellbar zu lagern.
- Horizontalformvorrichtung nach Anspruch 6, dadurch gekennzeichnet, dass die Formschenkel (36a-36d) der Formführungseinheit (18a-18d) einen in Transportrichtung (38a-38d) des Verpackungsmaterialschlauchs (16a) V-förmig zulaufenden Führungsbereich (40a-40d) ausbilden, der dazu vorgesehen ist, miteinander zu siegelnde Nahtbereiche des Verpackungsmaterialschlauchs (16a) zusammenzuführen.
- Horizontalformvorrichtung nach einem der vorhergehenden Ansprüche, gekennzeichnet durch zumindest eine Heizeinheit (42b), die dazu vorgesehen ist, die Formeinheit (12b) und/oder die Formführungseinheit (18b) zumindest abschnittsweise zu erhitzen, insbesondere zu einem Wärmeeintrag in einen Nahtbereich.
- Horizontalformvorrichtung nach einem der vorhergehenden Ansprüche, gekennzeichnet durch zumindest eine Luftdruckeinheit (44c), die dazu vorgesehen ist, an der Formeinheit (12c) und/oder an der Formführungseinheit (18c) einen Unterdruck und/oder einen Überdruck auf ein Verpackungsmaterial auszuüben.
- Horizontalformvorrichtung nach einem der vorhergehenden Ansprüche, gekennzeichnet durch zumindest eine angetriebene Andruckeinheit (48d), insbesondere eine Andruckrolle, die dazu vorgesehen ist, ein Verpackungsmaterial mit einer Andruckkraft gegen die Formführungseinheit (18d) zu beaufschlagen.
- Horizontalformvorrichtung nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Formeinheit (12a-12d) als Formschulter ausgebildet ist und die Formführungseinheit (18a-18d) als weitere Formschulter ausgebildet ist.
- Horizontalformvorrichtung nach Anspruch 3 und/oder 11, dadurch gekennzeichnet, dass die Formführungseinheit (18a-18d) zumindest zwei Formschenkel (36a-36d) umfasst, die relativ zueinander verstellbar, insbesondere linearbeweglich und/oder schwenkbeweglich, gelagert sind.
- Verpackungsmaschine, insbesondere horizontale Schlauchbeutelmaschine, mit zumindest einer Horizontalformvorrichtung nach einem der vorhergehenden Ansprüche.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102019132878.0A DE102019132878A1 (de) | 2019-12-03 | 2019-12-03 | Horizontalformvorrichtung |
| PCT/EP2020/083974 WO2021110604A1 (de) | 2019-12-03 | 2020-11-30 | Horizontalformvorrichtung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP4069593A1 EP4069593A1 (de) | 2022-10-12 |
| EP4069593B1 true EP4069593B1 (de) | 2023-09-27 |
Family
ID=73654829
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20816976.3A Active EP4069593B1 (de) | 2019-12-03 | 2020-11-30 | Horizontalformvorrichtung |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US12319526B2 (de) |
| EP (1) | EP4069593B1 (de) |
| JP (1) | JP7397198B2 (de) |
| CN (1) | CN114746339B (de) |
| DE (1) | DE102019132878A1 (de) |
| DK (1) | DK4069593T3 (de) |
| WO (1) | WO2021110604A1 (de) |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102020101759A1 (de) | 2020-01-24 | 2021-07-29 | Syntegon Packaging Systems Ag | Erstverpackung zu einer Aufnahme zumindest eines Produkts, insbesondere eines Lebensmittels |
| IT202000014857A1 (it) * | 2020-06-22 | 2021-12-22 | Ilapak Int S A | Gruppo piegatore per la piegatura di un materiale in film a formare un involucro tubolare. |
| IT202100026198A1 (it) * | 2021-10-13 | 2023-04-13 | Ilapak Int S A | Apparecchiatura confezionatrice orizzontale. |
| DE102022118077A1 (de) | 2022-07-19 | 2024-01-25 | Syntegon Packaging Systems Ag | Verpackungsformvorrichtung sowie Verpackungsmaschine |
| DE102023118754A1 (de) | 2023-07-14 | 2025-01-16 | Syntegon Packaging Systems Ag | Horizontalformvorrichtung, Verpackungsmaschine mit einer derartigen Horizontalformvorrichtung sowie Stützeinheit für eine derartige Horizontalformvorrichtung |
Family Cites Families (22)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1586334B1 (de) * | 1967-10-19 | 1972-03-16 | Nagema Veb K | Faltvorrichtung zum Umformen einer ebenen Folienbahn in einen Huellschlauch |
| JPS5633705Y2 (de) * | 1977-03-25 | 1981-08-10 | ||
| JPS577601Y2 (de) * | 1977-09-12 | 1982-02-13 | ||
| JPS55143494U (de) | 1979-03-31 | 1980-10-14 | ||
| JPS5767903U (de) * | 1980-10-07 | 1982-04-23 | ||
| US4520615A (en) * | 1983-02-28 | 1985-06-04 | Doboy Packaging Machinery, Inc. | Tube forming apparatus for packaging |
| JP2597441B2 (ja) * | 1992-03-31 | 1997-04-09 | 株式会社ハナガタ | 半折りフィルム等の合成樹脂包装材料による連続包装機 |
| US5255495A (en) * | 1992-10-30 | 1993-10-26 | Hayssen Manufacturing Company | Adjustable girth former |
| JP2567556B2 (ja) * | 1993-04-27 | 1996-12-25 | 株式会社ハナガタ | 帯状包装材料による連続包装機 |
| JP2854251B2 (ja) * | 1994-10-25 | 1999-02-03 | 株式会社フジキカイ | 横型製袋充填包装機におけるフイルム製袋装置 |
| DE19618559A1 (de) * | 1996-05-09 | 1997-11-13 | Kallfass Gmbh | Verpackungsmaschine |
| JP3002771B2 (ja) * | 1996-06-25 | 2000-01-24 | 株式会社フジキカイ | 横型製袋充填機のフィルム製袋装置 |
| JP3713108B2 (ja) * | 1996-08-14 | 2005-11-02 | 富士写真フイルム株式会社 | ピロータイプ包装装置 |
| FR2820361B1 (fr) * | 2001-02-02 | 2003-07-25 | Flexico France Sarl | Procede de fabrication de sachets a profiles de fermeture complementaires, machine et sachets obtenus |
| US6745545B2 (en) * | 2001-06-20 | 2004-06-08 | Illinois Tool Works Inc. | Horizontal form, fill and seal machine for loose fitting packages |
| JP2004035084A (ja) * | 2002-07-05 | 2004-02-05 | Fuji Photo Film Co Ltd | 包装袋のシーリング方法及びシーリング機構 |
| JP2005228871A (ja) | 2004-02-12 | 2005-08-25 | Seiko Epson Corp | 実装構造体、電気光学装置及び電子機器 |
| CN101177171B (zh) | 2007-08-22 | 2010-04-21 | 张建军 | 袋中袋全自动成型包装机 |
| CH699875A1 (de) * | 2008-11-13 | 2010-05-14 | Ferag Ag | Vorrichtung und verfahren zur bildung eines schlauchs aus einer materialbahn. |
| CN104309842B (zh) * | 2014-09-03 | 2016-06-15 | 成都松川雷博机械设备有限公司 | 一种适用于物料包装机的半成品成型方法 |
| CN105857668B (zh) * | 2016-06-01 | 2018-03-20 | 倪舒婷 | 一种枕形袋的成型结构及其枕形袋的成型工艺 |
| CN109353596A (zh) | 2018-11-01 | 2019-02-19 | 青岛海科佳电子设备制造有限公司 | 宽度可调包装袋成型器、制袋器、包装机及方法 |
-
2019
- 2019-12-03 DE DE102019132878.0A patent/DE102019132878A1/de not_active Withdrawn
-
2020
- 2020-11-30 US US17/781,807 patent/US12319526B2/en active Active
- 2020-11-30 WO PCT/EP2020/083974 patent/WO2021110604A1/de not_active Ceased
- 2020-11-30 EP EP20816976.3A patent/EP4069593B1/de active Active
- 2020-11-30 JP JP2022533353A patent/JP7397198B2/ja active Active
- 2020-11-30 DK DK20816976.3T patent/DK4069593T3/da active
- 2020-11-30 CN CN202080083281.5A patent/CN114746339B/zh active Active
Also Published As
| Publication number | Publication date |
|---|---|
| BR112022010164A2 (pt) | 2022-08-09 |
| EP4069593A1 (de) | 2022-10-12 |
| WO2021110604A1 (de) | 2021-06-10 |
| JP2023509298A (ja) | 2023-03-08 |
| US12319526B2 (en) | 2025-06-03 |
| DE102019132878A1 (de) | 2021-06-10 |
| CN114746339A (zh) | 2022-07-12 |
| DK4069593T3 (da) | 2023-12-18 |
| CN114746339B (zh) | 2023-10-27 |
| US20230174332A1 (en) | 2023-06-08 |
| JP7397198B2 (ja) | 2023-12-12 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE102019132878A1 (de) | Horizontalformvorrichtung | |
| DE69117095T2 (de) | Strömungsmittelbetätigte Vorrichtung und Verfahren zur Stabilisierung | |
| EP4143095B1 (de) | Horizontalformvorrichtung | |
| EP0735979B1 (de) | Verfahren und vorrichtung zum herstellen eines längsfalzes | |
| EP0899228B1 (de) | Luftpolsterführung | |
| DE3327462A1 (de) | Verfahren und vorrichtung zum abdecken der offenen schnittkante eines kartonzuschnittes | |
| WO2018059730A1 (de) | Verfahren und vorrichtung zum zuführen von wäschestücken zu einer wäschebehandlungseinrichtung, insbesondere einer mangel | |
| EP0240827A1 (de) | Vorrichtung zur Herstellung von Luftpolster-Versandtaschen | |
| EP0285855A1 (de) | Verfahren und Vorrichtung zum Verpacken von Gegenständen mit einer bahnförmigen Kunststoffolie | |
| EP3070009A1 (de) | Vorrichtung und verfahren zur herstellung von folienschrumpfgebinden | |
| WO2006108377A1 (de) | Verfahren und vorrichtung zum ablegen einer flexiblen materialbahn | |
| EP3269539B1 (de) | Vorrichtung zum öffnen eines endbereichs eines schlauchförmigen sackkörpers | |
| EP0806346A2 (de) | Mit einer Schlauchformeinrichtung versehene Verpackungsmaschine | |
| EP2711164B1 (de) | Vorrichtung und Verfahren zum Öffnen eines Endbereichs eines schlauchförmigen Sackkörpers | |
| DE2255768B2 (de) | Verfahren und vorrichtung zum herstellen von klotzbodenbeuteln aus heissiegelfaehigem material | |
| DE102008017443B4 (de) | Vorrichtung und Verfahren zur Herstellung von Säcken aus Schlauchstücken | |
| DE102013014732B4 (de) | Verfahren und Vorrichtung zur Herstellung von Kreuzboden-Säcken | |
| DE69500781T2 (de) | Luftleitflügel für eine pneumatische Wendestange | |
| DE19515718A1 (de) | Vorrichtung zum Verpacken von Gegenständen in einen Schlauchbeutel | |
| DE1461916A1 (de) | Maschine zum Herstellen,Fuellen und Verschliessen von Packungen | |
| DE69702108T2 (de) | Verfahren und Apparat zur kontaktlosen Verzögerung von flachen Produkten | |
| DE10134255B4 (de) | Verpackungsmaschine | |
| DE2420970A1 (de) | Verfahren zur herstellung von beuteln und vorrichtung zur durchfuehrung des verfahrens | |
| DE102023118754A1 (de) | Horizontalformvorrichtung, Verpackungsmaschine mit einer derartigen Horizontalformvorrichtung sowie Stützeinheit für eine derartige Horizontalformvorrichtung | |
| DE1144175B (de) | Verfahren und Vorrichtung zum Zufuehren flachgelegter Beutel zu einer Verwendungsstelle, z. B. einer Fuellmaschine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: UNKNOWN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20220629 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20230419 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502020005451 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 Effective date: 20231214 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20231228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20231227 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20231228 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240127 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240127 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502020005451 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20231130 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20240628 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20201130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20201130 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: U11 Free format text: ST27 STATUS EVENT CODE: U-0-0-U10-U11 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20251201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230927 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20251119 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251118 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20251120 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20260113 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20251128 Year of fee payment: 6 Ref country code: DK Payment date: 20251119 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20251201 Year of fee payment: 6 |