EP3395703B1 - Verfahren und vorrichtung zum applizieren von packhilfsmitteln - Google Patents
Verfahren und vorrichtung zum applizieren von packhilfsmitteln Download PDFInfo
- Publication number
- EP3395703B1 EP3395703B1 EP17020177.6A EP17020177A EP3395703B1 EP 3395703 B1 EP3395703 B1 EP 3395703B1 EP 17020177 A EP17020177 A EP 17020177A EP 3395703 B1 EP3395703 B1 EP 3395703B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- application
- packaging materials
- transfer
- additive packaging
- packaging
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
- B65B61/20—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for adding cards, coupons or other inserts to package contents
- B65B61/205—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for adding cards, coupons or other inserts to package contents for adding drinking straws to a container
Definitions
- the invention relates to a device for the separate application of packaging aids supplied as an endless strip of packaging aids, preferably repackaged straws, to packs, in particular composite carton packs, with a separating element for separating the packaging aids of the endless strip of packaging aids, a feed means for feeding the endless strip of packaging aids to the separating element and for passing on the packaging aids separated by the separating element, an application means for applying the separated packaging aids to the packs and a transport means for transporting the packs along a pack transport path to the application means.
- the invention also relates to a method for the separate application of packaging aids, preferably repackaged straws, supplied as an endless strip of packaging aids, to packs, in particular composite cardboard packs.
- Packaged goods are packaged using packaging.
- Packaged goods and packaging together form a package.
- composite packs are also used for filling and packaging products that can flow, in particular, such as beverages or other foods.
- Composite packs are formed from packaging materials that are connected to one another.
- packaging material cardboard composite carton packs also have the packaging material plastic, for example. Cardboard and plastic are connected to each other over a large area and form a so-called packaging laminate as a layered structure.
- the cardboard layer gives the pack stability and serves as a carrier layer for plastic layers.
- Plastic layers serve, among other things, as liquid barriers, so that packaged goods such as free-flowing products, for example beverages, can be filled and so that no moisture can penetrate into the cardboard layer from the outside.
- layers of plastic can be sealed as thermoplastic layers.
- materially joined sealing seams are used to form the packaging and to close it pack possible.
- the layer structure of the packaging laminate can vary depending on the requirements. For example, an aluminum layer is additionally inserted for aseptic filling goods in order to achieve a good barrier effect against gases and light.
- grooves are often made in the packaging laminate. Grooves define the future fold lines. The folds form the pack edges on the pack and/or enable the pack bottom and/or pack top to be formed.
- Packaging laminates are also usually printed with a decor.
- the pack laminate is cut to the interval of a pack during its manufacture.
- Such blanks can be further processed into what are known as packing jacket blanks.
- the blank is folded over and connected to form a tube with a longitudinal sealing seam.
- Such packaging shell blanks form the actual packaging of a carton composite pack.
- the packaging laminate can be provided as a continuous material, in particular as rolled goods.
- a packaging machine which is often referred to as a form/fill machine, in reference to its main functions, in particular forming the pack, filling the pack and sealing the pack.
- a form/fill machine in reference to its main functions, in particular forming the pack, filling the pack and sealing the pack.
- /Seal machine Liquid foods such as beverages, soups or yoghurt are primarily considered as filling goods. Also conceivable are coagulated, pasty and chunky products or free-flowing products with chunky portions, which can also preferably be food.
- the carton composite packs are also referred to as beverage carton composite packs.
- Packs of the type mentioned are sometimes also provided with packaging aids such as pouring elements and/or straws, which are also referred to as drinking straws.
- the latter are usually - in order to ensure the necessary hygiene - included in sealed outer packaging.
- the Packaging aids can be glued to a side wall of a carton composite pack, for example by means of hot glue. If the consumer wants to consume the product with a straw, he first removes the wrapped straw from the side wall of the pack, in particular the composite carton pack, and peels it out of the outer packaging. The exposed straw can then be pushed at the pointed end into a specially weakened area in the pack, in particular the composite carton pack, so that the product can be consumed directly through the straw.
- Packing aids are commercially available as bulk goods in the form of endless tapes.
- An endless belt of packaging aids is generally made up of a large number of packaging aids connected to one another in the direction of the belt, from which packaging aids are separated or individualized in sequence and then applied to the packs.
- endless straw strips these are formed, for example, by straws that are aligned transversely to the direction of the strip and are welded into foil.
- the film forms both the respective outer packaging of the straws and - in their sequence - the "endless" band.
- the endless band of straw is fed from a supply roll via deflection rollers into a clocked-driven supply means in order to feed the endless band to a separating element for separating the straws and to pass the separated straws on to an application means.
- the repackaged straws are separated in the supply means by means of a cutting knife that can be moved back and forth and then moved further in the direction of the application site.
- the filled and closed cardboard composite packs are meanwhile provided with adhesive by a transport means along a linear transport path and fed to an application means.
- the individual straws are applied by the application means to the supplied packs at the application site by means of a transfer element.
- the timing of Feeding means allows the straws to be separated when they are stationary. However, this cyclical approach often has a limiting effect on the processing speeds.
- the European patent EP 1 042 172 B1 proposes a device for attaching repackaged straws to composite carton packs, the endless belt being fed to a continuously rotating feed means, where the separation of the straws from the endless belt is accomplished by severing the endless belt by means of a separating means.
- the feeding means first feeds in the endless belt, in order then to separate the straws by means of a separating means in the form of a cutting knife.
- the cutting blade In addition to a radial piercing movement in the direction of the axis of rotation of the drive means, the cutting blade also performs a following movement over a certain peripheral section of the feed means.
- the straws separated in this way are passed on to an application means in the form of an application fork, which also moves continuously, by which the straws are pressed onto the packs which have previously been provided with adhesive and are brought along a transport path via a transport means.
- Separating means running partly over the circumference of the feed means are mechanically complex and relatively prone to failure. They also often produce unsatisfactory cutting results such as protruding dividing brows or the like.
- the pamphlet EP 0 350 590 A1 describes an apparatus and method for attaching a packaged drinking straw to a package, the packages being transportable on a conveyor which is continuously movable at a first speed.
- Drinking straws move over a first deflection roller and are processed by a cutting station in such a way that individual, packaged drinking straws are produced.
- the straws are taken from a reciprocating carriage, accelerated to a speed and transferred by a transfer finger to a tong chain running at the same speed.
- the mechanism of the tong chain attaches the drinking straws to packages, which are conveyed on package conveyors at the same speed.
- the pamphlet JP S60 172627 A describes an apparatus for applying straws to packages, the apparatus comprising first, second and third drums. On the first intermittently rotating drum, straws are severed from a continuous belt and one at a time, transferred to a second faster rotating drum, transferred from the second drum to an even faster rotating third drum, and up from the third drum packaging applied.
- the three drums are connected to each other via a gearbox. Proceeding from this, it is the object of the present invention to design and develop a device and a method of the type mentioned at the outset and described in more detail above in such a way that the disadvantages described are overcome. In particular, the separation and application of packaging aids should be quick, reliable and of high quality.
- a transfer means for taking over the packaging aids passed on by the feeding means and for accelerating the taken over Packaging aids is provided at a speed adapted to the application means.
- a transfer means interposed between the supply and application means allows a functional and structural decoupling of the separation of the packaging aids from the endless belt of packaging aids and the application of the separated packaging aids to the packs.
- the packaging aids can be separated and applied to the packs at different speeds, each in accordance with the requirements.
- the transfer means as a bridging element also enables the packaging aids to be transferred safely from the separation site to the application site, even at the highest application speeds.
- the transfer means can take over the separated packaging aids directly from the supply means and/or transfer them directly to the application means.
- the supply means and the application means are then coupled directly via the transfer means, so that further assemblies are unnecessary.
- this also means that the packaging aids are taken over at one point, the takeover position, of the transfer means and transferred to the application means at another point, the transfer position of the transfer means.
- the takeover and the handover preferably take place one after the other, in particular alternately, in order to be able to implement the takeover and the handover at different speeds.
- the transfer means as a whole can be accelerated or decelerated.
- the transfer means can be braked and another part of the transfer means can be accelerated, if necessary.
- carriers can be provided for receiving the packaging aids, which can be braked and accelerated independently of one another. The carriers are then, for example, decelerated before the packaging aids are taken over and accelerated before the packaging aids are handed over. If the transfer means is accelerated or decelerated overall, so-called smoldering operation comes into question.
- the transfer means can rotate slowly or even stand still and take over a packaging aid from the feed means.
- the feed means can then be accelerated in order to transfer the packaging aid or another packaging aid to the application means at a higher speed, after which the transfer means is decelerated again in order to take over another packaging aid.
- the packaging aids can be transported in a horizontal and/or vertical direction.
- an endless belt of packaging aids is first fed to the supply means, which has the packaging aids in sequence.
- the feeding means feeds the endless belt of packaging aids to a separating element, which separates the endless belt of packaging aids and thereby separates and separates the individual packaging aids of the endless belt of packaging aids.
- the packaging aids which are now present individually and separately, are transported away from the separating element by the feeding means and towards a transfer means.
- the transfer means takes over the packaging aids at a position spaced apart from the separating member at a low speed or, if necessary, at a speed of zero.
- the packaging aids are transported further by the transfer means in the direction of an application means, with the packaging aids being accelerated before being transferred to the application means in order to then be transferred from the transfer means to the application means at a higher speed than when the packaging aids are taken over.
- This higher speed is matched to the speed of the application means that is moved in order to apply the packaging aids to packs that are moved past the application means via a transport means along a pack transport path and during which the individual packaging aids are received.
- the feed means for the step-by-step transport of the packaging aids can be driven in a clocked manner. Since the individual packaging aids typically follow one another at fixed intervals on the endless belt of packaging aids, it makes sense to also supply them at timed intervals. A work cycle tailored to the packaging aids enables further work processes to be carried out. In this way, a very precise and reproducible feeding of the packaging aids can be achieved. Alternatively or additionally, it is achieved in a simple manner that the packaging aids can be separated from the endless belt of packaging aids while the endless belt or the feed means is stationary or only moving at a low speed.
- the separating member is designed to be driven in a clocked manner, the work steps of separating and feeding can be optimally coordinated with one another. In this way, a very precise and reproducible separation of the packaging aids can be achieved, which can be done as needed while the endless belt or the feed means is stationary or moving only at low speed. This leads to trouble-free separation and isolation of the packaging aids, so that operational disruptions are minimized.
- the clocking of the separating element can consist in the separating element being repeatedly moved back and forth in opposite directions. However, the clocking can preferably also take place in such a way that the separating element is stopped for a short period of time in an end position spaced apart from the endless belt of packaging aids. It is also particularly expedient for the reliability and the process management if the separating element can be driven synchronously with the feed means.
- the feed means is preferably designed as or includes a rotatable carousel with receptacles distributed over the circumference for transporting the packaging aids to the separating element and for passing on the packaging aids.
- a rotatable carousel with receptacles distributed over the circumference for transporting the packaging aids to the separating element and for passing on the packaging aids.
- the receptacles are advantageously designed to correspond to the shape of the packaging aids, so that the receptacles can receive the packaging aids in a form-fitting manner and hold them appropriately.
- the diameter and division, ie the number of recordings related to the circumference, of the carousel can be matched to the work processes in such a way that the performance and function of the device are improved. Furthermore, the packaging aids can also be transported very easily and reliably, with installation space being able to be saved if required.
- Structurally advantageous, radial notches are incorporated between the receptacles to accommodate the separating element when separating the packaging aids, so that the separating element, for example in the form of a cutting blade, can briefly dip into the notch during the separation process and thereby cut through the endless belt of packaging aids, while preferably the adjacent packaging aids are positively included in the recordings.
- the endless belt of packaging aids has a certain pretension, which simplifies the separation of the packaging aids and improves the quality and safety of the separation.
- the application means has a drivable application wheel.
- the packaging aids can be transported precisely and quickly to the application site without the need for more equipment. This is particularly the case since the application wheel can be driven at a substantially constant rotational speed.
- the reliability of the application is improved if the peripheral speed of the application wheel corresponds at least essentially to the transport speed of the packs along the transport path at the application site. In this way, a low relative speed between the packs and the packaging aids when they are applied can be ensured, so that a process-stable application with fewer rejects is possible. If the speeds are as constant as possible, unwanted forces resulting from acceleration are minimized.
- the transfer means has a transfer wheel that can be rotated at varying circumferential speeds. Varying speeds of the transfer device that are adapted to the circumstances improve the robustness of the processes, especially when the packaging aids are accepted and handed over by the transfer device.
- the packaging aids can be accepted at a suitable speed of the transfer device and the packaging aids can be transferred at another suitable speed of the transfer device, in order to optimize the overall process, for example.
- the carousel and the transfer means are particularly advantageously designed in such a way that for the transfer of the packaging aids from the carousel to the transfer means, the carousel and the transfer means are at least approximately stationary or only move at low speed. Such a configuration increases process reliability and avoids disruptions when taking over the packaging aid.
- the transport means can be assigned at least one adhesive application means for gluing the packs fed to the application means along the pack transport path. If the adhesive is applied directly to the packs in a separate process step, unwanted sticking of functional and subassemblies is prevented and stable operation of the device is thus achieved.
- the feed means and the transfer means are driven in a clocked manner.
- the same can apply to the transfer means if the packaging aids are taken over by the transfer means when the transfer means is at a standstill. Otherwise, the speed of the transfer means can be increased and reduced again cyclically, without it leading to The transfer means comes to a standstill.
- the application means moves continuously at at least a substantially constant speed. In addition, the speed is preferably quite high in order to enable a large throughput of packages. This is easily and reliably possible if the application means does not have to be decelerated and accelerated again every time between two applications.
- a packaging aid is preferably separated when the feeding means stops at least once, in particular when the feeding means stops. If the packaging aids are taken over by the transfer means when the feed means is moving slowly, the packaging aids can be passed on briefly before or after the feed means has come to a standstill, during which the speed of the feed means is low anyway. In any case, this simplifies the operation and the feeding means does not have to be stopped as often.
- the transfer means can receive the individual packaging aids that have been passed on directly or indirectly from the supply means.
- the former is structurally easier to accomplish and can take place at a transfer position that can be identical for all packaging aids.
- the supply means can transfer the separated packaging aids to the transfer means, it being possible for the transfer to take place while the supply means and the transfer means are moving, in particular rotating.
- the turning can be regarded as a movement around an axis of rotation. However, turning can also be viewed as moving along a closed path, where the path may or may not be circular.
- the feed means is formed by a carousel or the feed means has a carousel which rotates around a central axis of rotation at a cyclically varying speed.
- the transfer means can be designed as a transfer wheel or have a transfer wheel. The transfer wheel then preferably rotates at a cyclically varying speed about a central axis of rotation. The axes of rotation are preferably aligned parallel to one another in order to standardize the rotary movements.
- the carousel and the transfer wheel can be moved at least essentially the same peripheral speed when taking over a packaging aid, so that the packaging aid has an at least essentially constant speed when it is passed on.
- the application means represents an application wheel or includes an application wheel.
- the application means can thus be moved at a constant speed without any problems by causing the application wheel to rotate at a constant rate.
- the rotation or the peripheral speed of the application wheel is then, in a simple manner, at least essentially the same when the packaging aids are taken over and when the packaging aids are applied.
- the packaging aids are thus moved by the application wheel at a constant speed, as required, from the point at which the packaging aids are taken over to the point of application.
- the transfer wheel is accelerated to the peripheral speed of the application wheel after the transfer of a packaging aid from the feed means.
- the packaging aid can then be passed on from the transfer wheel to the application wheel, at least essentially without any change in speed.
- the packaging aids are transported at a speed, in particular peripheral speed, from the transfer means to the Pass on application agents, which corresponds at least essentially to the speed, in particular peripheral speed, at which the packaging aids are applied to the packs. This can be done easily and reliably.
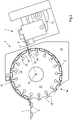
- the Figure 1A shows a device 1 for applying packaging aids 2 in the form of repackaged straws 3 to already filled and sealed packs 4 in the form of carton composite packs, which are designed here as beverage carton composite packs.
- the packaging aids 2 are in the form of a Packing aids endless strip 5 drawn from a feed means 6 in the device 1, which feeds the packaging aids endless strip 5 of a separating device 7.
- the separating device 7 separates the endless belt 5 of packaging aids into individual packaging aids 2, which are transported further by the feed means 6 to a transfer means 8, from which the packaging aids 2 are taken over individually and one after the other.
- This transfer of the packaging aids 2 takes place at a low speed of the transfer means 8 or the packaging aids 2.
- the packaging aids 2 are transferred from the transfer means 8 to an application means 9, with the transfer means 8 having been accelerated in the meantime, so that the transfer of the Packaging aids 2 to the application means 9 takes place at a significantly higher speed.
- the application means 9 applies the packaging aids 2 passed on from the transfer means 8 to the application means 9 in an application position 19 in sequence to the packs 4 transported past the application position 19.
- the transport of the packs 4 along a pack transport path 10 and past the application means 9 takes place with the aid of a transport means 11.
- the packs 4 are transported by the transport means 11 at a constant speed past the application means 9, in particular at the application position 19.
- the transport means 11 which is shown and is preferred in this respect has a transport belt 14 which is provided with cams 13 and which extends in the transport direction of the packs 4 .
- the individual cams 13 are positively engaged with the packs 4 and move the packs 4 at defined intervals and at a defined speed along the application means 9.
- the application means 9 is designed as an application wheel 1 in the embodiment shown and is preferred in this respect, which has a plurality of applicators 17 rotating about the axis of rotation 16 of the application wheel 15 and distributed uniformly over the circumference of the application wheel 15 .
- the applicators 17 At a transfer position 18, the applicators 17 each accept a packaging aid 2 and spend this to the application position 19 in order to apply it there to a pack 4 transported past.
- connection between packaging aid 2 and pack 4 is given in the illustrated embodiment by an adhesive bond, with other connections are also conceivable.
- Hot melt is used as the adhesive, which is applied selectively to the sides 12 of the packages 4 by means of adhesive application means 20 arranged on a package transport path 10, in particular in the form of adhesive application nozzles.
- adhesive application means 20 arranged on a package transport path 10, in particular in the form of adhesive application nozzles.
- a packaging aid 2 is pressed into the hot glue points.
- a pressure belt 22 presses the freshly applied packaging aids 2 against the packs 4 over a certain distance immediately from the application position 19, while the packs 4 are transported onwards.
- the packaging aids 2 are supplied to the device 1 in the form of a packaging aids endless belt 5, which is partly in the Figure 1B is shown in more detail, and applied to packs 4 after separation.
- the packaging aids 2 are composed of a straw 3 and two foils 23 . Different shapes can be used as straws 3, but in particular they are at least partially U-shaped or I-shaped straws 3 Edges 24 are welded and form a pocket 25 in between, in which the straw 3 is accommodated. In other words, the straw 3 is wrapped in foil 23 .
- the endless belt 5 of packaging aids is formed by arranging the packaging aids 2 in a row, with the foils of adjacent packaging aids 2 being connected to one another in each case.
- the straws 3 are received between two films extending along the entire endless belt of packaging aids 5 .
- the endless band of packaging aids 5 represents an "endless" sequence of packaging aid units.
- a pack 4 with a on it applied and separated from the packaging aids endless belt 5 packaging aids 2 is in the Figure 1C shown as an example.
- the packaging aid 2 is applied approximately diagonally to the associated side 12 of the pack 4, but this does not necessarily have to be the case.
- the packs 4 that are shown and are preferred in this respect have a free-flowing foodstuff, in particular a beverage.
- pack 4 is a carton composite pack, and therefore a beverage carton composite pack.
- the packaging is formed from a packaging laminate that includes layers of different packaging materials, namely at least cardboard and plastic.
- the plastic layers are provided on the outside of the packaging laminate and are formed from thermoplastics, in particular polyethylene (PE).
- PE polyethylene
- the pack 4 is formed and closed by folding and sealing the pack laminate. If required, the packaging laminate is printed with a decoration on one side.
- the supply means 6 comprises a carousel 27 which rotates clockwise about a central axis of rotation 26 and which has receptacles 28 distributed over its circumference for the partial receptacle 28 of the packaging aids 2 .
- the receptacles 28 are modeled on the shapes of the straws 3 so that the straws 3 and thus the packaging aids 2 are held in the receptacles 28 in a form-fitting manner. So that the packaging aids 2 remain in the receptacles 28, a stationary side wall 21 is provided on the peripheral side.
- a torsion spring-loaded clamping plate 30 is provided in the area where the endless belt 5 of packaging aids is pulled in by the feed means 6 , which guides the endless belt of packaging aids 5 on the peripheral side and presses it against the carousel 27 and into the receptacles 28 .
- the clamping plate 30 transitions into the side wall 21 as seen in the transport direction of the endless belt 5 of packaging aids. If a new endless belt 5 of packaging aids is to be inserted, the clamping plate 30 can be swiveled outwards and locked in place in order to simplify the insertion of the endless belt 5 of packaging aids.
- the feed means 6 that is shown and is preferred in this respect is carried out the carousel 27 with the receptacles 28, the side wall 21 and the clamping plate 30 is formed.
- a separating device 7 for separating the packaging aids 2 from the endless belt of packaging aids 5 with a separating element 31 is assigned to the feed means 6.
- the separating element 31 is moved radially at least essentially in the direction of the axis of rotation 26 of the carousel in the illustrated and therefore preferred device 1 with a drive mechanism 32 27 moves back and forth, as indicated by the double arrow.
- the separating element 31 is designed as a sharpened cutting blade on the edge 33 assigned to the endless belt of packaging aids 5 and cuts through the endless belt of packaging aids 5 in the connection area of two consecutive packing aids 2, as a result of which the packaging aids 2 of the endless belt of packaging aids 5 are separated from one another or isolated one after the other.
- the separating member 31 engages at least partially in notches 34 arranged along the circumference of the carousel 27 between the receptacles 28 for the packaging aids 2 .
- the carousel 27 works in a clocked mode, in which the carousel 27 is stopped in cycles and rotated further by a circumferential segment that corresponds to the width of a packaging aid 2 .
- the carousel 27 is synchronized with the drive mechanism 32 of the separating device 7 such that when the carousel 27 is stationary, the separating member 31 is moved forward in the direction of the axis of rotation 26 of the carousel 27 and back to the starting position.
- the separating element 31 severs the endless belt of packaging aids 5 in the region of the associated notch 34.
- the carousel 27 rotates in one go further cycle to the next position, as a result of which the separating member 31 faces the next notch 34 and can separate the next packaging aid 2 from the endless belt 5 of packaging aids by moving it forward.
- the separating device 7 is stationarily arranged on the feeding means 6 and only the separating member 31 moves back and forth, in one linear and based on the carousel 27 radial movement. A cyclic adjustment of the separating element 31 in the circumferential direction does not take place in the case of the separating element 31 that is shown and is preferred in this respect.
- the notches 34 end in the radial direction in vertically extending drainage channels 35, which have a larger cross section than the width of the notches 34 adjacent to the emptying channels 35.
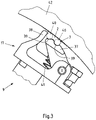
- the application means 9 comprising an applicator 17 is shown.
- the application finger 37 has two grooves 39 on the face side, which correspond to the shape of the packaging aid 2 , in particular the straw 3 .
- the two grooves 39 are used to hold the two legs 40 of the U-shaped straw 3, as is shown by a packaging aid shown in dashed lines together with a straw 3.
- one groove 39 would basically be sufficient.
- the application finger 37 can be pivoted slightly against the spring force of a spring 41 and is configured in such a way that the packaging aid 2 is clamped between the transfer position 18 and the application position 19 between the application finger 37, the guide finger 38 and a side rail 42 provided on the circumference of the application wheel 15 and is therefore guided safely.
- the guide finger 38 prevents the packaging aid 2 from disengaging from the application finger 37 in the circumferential direction.
- the application wheel 15 shown also has an adjustment mechanism - not described in detail here - which allows the packaging aids 2 to be pivoted about a radial axis between the transfer position 18 and the application position 19 in such a way that the packaging aids 2 in the transfer position 18 are parallel to the axis of rotation 16 of the application wheel 15 can be taken over and applied diagonally to the associated side 12 of the associated pack 4, as in FIG Figure 1C is shown.
- the application wheel 15 rotates at such a constant angular speed or circumferential speed that the packaging aids 2 or the applicators 17 have a circumferential speed at the end face at the application position 19 that is at least approximately the speed of the packs 4 in terms of magnitude and direction correspond to the application position 19.
- Such an operation minimizes relative speeds between pack 4 and packaging aid 2 during application.
- a transfer means 8 with a transfer wheel 44 rotatable about an axis of rotation 43 and a further side wall 29 provided on the circumference, as is shown in detail in FIG 4 is shown.
- the transfer wheel 44 has elongated receiving grooves 45 for receiving the packaging aids 2, which are distributed evenly over the circumference of the transfer wheel 44.
- the packaging aids 2 and the endless belt 5 of packaging aids are not shown.
- the packaging aids 2 are guided between the transfer wheel 44 and the stationary additional side wall 29 and are transported in the circumferential direction by the form fit between the receiving grooves 45 and the packaging aids 2 .
- the transfer means 8 takes over the passed on packaging aid 2 from the carousel 27 and accelerates the packaging aid 2 between the transfer position 36 and the transfer position 18 to a speed adapted to the application wheel 15 and transfers the packaging aid 2 to an applicator 17 of the application wheel 15 at the transfer position 18.
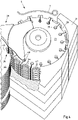
- the part of the transfer means 8 is shown which is located in the area of the transfer position 36 of the packaging aid 2 from the carousel 27 to the transfer wheel 44 of the transfer means 8.
- the carousel 27 is formed by a large number of stacked plate elements 46 spaced apart from one another, so that a plurality of intermediate levels 47 are formed between the plate elements 34 .
- Several fixed combing out lamellae 48 protrude into these intermediate levels 35 as extensions of the further side wall 21.
- the combing out lamellae 48 together form a sectional guide when the packaging aids 2 are guided out of the receptacles 28 of the carousel 27, so that with the further side wall 21 the packaging aid 2 has a uninterrupted leadership when taking over the packaging aid 2 in the receiving grooves 45 of the transfer wheel 44 from the recordings 2 of the carousel 27 is required.
- the transfer wheel 44 in the area of the receiving grooves 45 has a peripheral speed that is approximately the same, albeit low, as the carousel 27 in the area of the receptacles 28, so that the packaging aids 2 are at least essentially free of acceleration from the feed means 6 to the transfer means 8 can be passed on.
- the transfer wheel 44 is rotated further and in particular accelerated from the point in time at which the packaging aid 2 is received and guided between the transfer wheel 44 and the additional side wall 29 .
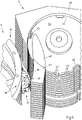
- the transfer means 8 and the application means 9 are shown in the area of the transfer position 18 .
- the transfer wheel 44 is constructed in a similar way to the carousel 27, namely from a plurality of plate elements 46, which in turn also form intermediate levels 47 into which a number of combing-out lamellae 49 protrude as a continuation of the side bands 42 . This allows the packaging aids 2 to be combed out of the receiving grooves 45 of the transfer wheel 44 in the area of the transfer position 18.
- the transfer wheel 44 and the applicator wheel 15 have at least approximately the same peripheral speeds.
- the packaging aid 2 is held by the application finger 37 and by the guide finger 38 .
- the combing-out lamellae 49 comb the packing aid 2 completely out of the receiving groove 45 and the packing aid 2 is guided through the side rails 42 and pressed against the side rails 42 as the rotation continues.
- the packaging aids 2 are transported by the applicator wheel 15 from the transfer position 18 to the application position 19 at a constant speed and are thereby pivoted about a radial axis. In the application position 19, the packaging aid 2 is then applied at an angle to the pack 4 transported past.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
Description
- Die Erfindung betrifft eine Vorrichtung zum separaten Applizieren von als Packhilfsmittel-Endlosband zugeführten Packhilfsmitteln, vorzugsweise umverpackten Strohhalmen, an Packungen, insbesondere Karton-Verbundpackungen, mit einem Trennorgan zum Vereinzeln der Packhilfsmittel des Packhilfsmittel-Endlosbandes, einem Zuführmittel zum Zuführen des Packhilfsmittel-Endlosbandes zum Trennorgan und zum Weitergeben der durch das Trennorgan vereinzelten Packhilfsmittel, einem Applikationsmittel zum Applizieren der vereinzelten Packhilfsmittel an die Packungen und einem Transportmittel zum Transportieren der Packungen entlang eines Packungs-Transportpfads zum Applikationsmittel. Die Erfindung betrifft zudem ein Verfahren zum separaten Applizieren von als Packhilfsmittel-Endlosband zugeführten Packhilfsmitteln, vorzugsweise umverpackten Strohhalmen, an Packungen, insbesondere Karton-Verbundpackungen.
- Packgüter werden mittels Verpackungen verpackt. Packgut und Verpackung bilden zusammen eine Packung. Zum Abfüllen und Verpacken von insbesondere fließfähigen Produkten, wie Getränken oder anderen Lebensmitteln, werden neben Flaschen und Dosen auch Verbundpackungen verwendet. Verbundpackungen sind aus miteinander verbundenen Packstoffen gebildet. Karton-Verbundpackungen weisen neben dem Packstoff Karton beispielsweise auch den Packstoff Kunststoff auf. Karton und Kunststoff sind flächig miteinander verbunden und bilden als Schichtaufbau ein sogenanntes Packungslaminat. Die Kartonschicht verleiht der Packung Stabilität und dient als Trägerschicht für Kunststoffschichten. Kunststoffschichten dienen unter anderem als Flüssigkeitssperren, so dass Packgüter wie fließfähige Produkte, beispielsweise Getränke, abgefüllt werden können und so dass keine Feuchtigkeit von außen in die Kartonschicht eindringen kann. Ferner lassen sich Kunststoffschichten als thermoplastische Schichten siegeln. So werden beispielsweise stoffschlüssig gefügte Siegelnähte zur Ausbildung der Verpackung und zum Verschließen zur Packung möglich. Der Schichtaufbau des Packungslaminats kann je nach Anforderungen variieren. So wird beispielsweise für aseptische Füllgüter zusätzlich eine Aluminiumschicht eingelegt, um eine gute Barrierewirkung gegen Gase und Licht zu erzielen. Um das flächige Packungslaminat falzen, also maschinell falten, zu können, sind oft Rillungen in das Packungslaminat eingebracht. Rillungen definieren die späteren Falzlinien vor. Die Falzungen bilden an der Packung die Packungskanten und/oder ermöglichen die Ausformung von Packungsboden und/oder Packungskopf. Packungslaminate sind zudem meist mit einem Dekor bedruckt.
- Oft - aber nicht immer - wird das Packungslaminat noch während seiner Herstellung auf das Intervall einer Verpackung zugeschnitten. Solche Zuschnitte können zu sogenannten Packungsmantelrohlingen weiterverarbeitet werden. Dabei wird der Zuschnitt umgelegt und durch eine Längssiegelnaht zu einem Rohr verbunden. Solche Packungsmantelrohlinge bilden das eigentliche Packmittel einer Karton-Verbundpackung. Alternativ kann das Packungslaminat als Endlosmaterial, insbesondere als Rollenware, bereitgestellt werden.
- Das eigentliche Formen und Befüllen der Verpackung und das Verschließen zu einer Packung geschieht in einer Verpackungsmaschine, die nicht selten in Anlehnung an ihre Hauptfunktionen, insbesondere das Formen der Verpackung, das Füllen der Verpackung und das Siegeln der Verpackung, auch als Form-/Fill-/Seal-Maschine bezeichnet wird. Als Füllgüter kommen vorwiegend flüssige Lebensmittel wie beispielsweise Getränke, Suppen oder Joghurt in Frage. Denkbar sind auch gestockte, pastöse und stückige Produkte oder fließfähige Produkte mit stückigen Anteilen, die ebenfalls vorzugsweise Lebensmittel sein können. Im Falle von Getränken werden die Karton-Verbundpackungen auch als Getränkekarton-Verbundpackungen bezeichnet.
- Packungen genannter Art werden zuweilen auch mit Packhilfsmitteln wie beispielsweise Ausgießelementen und/oder Strohhalmen, die auch als Trinkhalme bezeichnet werden, versehen. Letztere sind in der Regel - um die gebotene Hygiene zu gewährleisten - in verschlossenen Umverpackungen aufgenommen. Die Packhilfsmittel können beispielsweise mittels Heißleim an eine Seitenwand einer Karton-Verbundpackung geklebt sein. Will der Konsument das Produkt mit einem Strohhalm verzehren, entfernt er zunächst den umverpackten Strohhalm von der Seitenwand der Packung, insbesondere der Karton-Verbundpackung, und schält diesen aus der Umverpackung. Der freigelegte Strohhalm lässt sich sodann am gespitzten Ende in einen speziell geschwächten Bereich in der Packung, insbesondere der Karton-Verbundpackung, stoßen, so dass das Produkt direkt über den Strohhalm verzehrt werden kann.
- Als Massenware sind Packhilfsmittel marktüblich als Endlosbänder verfügbar. Ein Packhilfsmittel-Endlosband ist in der Regel aus einer Vielzahl von in Bandrichtung miteinander verbundenen Packhilfsmitteln aufgebaut, von denen der Reihe nach Packhilfsmittel separiert bzw. vereinzelt und anschließend an den Packungen appliziert werden. Im Falle von Strohhalm-Endlosbändern werden diese beispielsweise durch quer zur Bandrichtung ausgerichtete und in Folie eingeschweißte Strohhalme gebildet. Die Folie bildet dabei sowohl die jeweilige Umverpackung der Strohhalme wie auch - in ihrer Abfolge - das "endlose" Band.
- Für die maschinelle Vereinzelung und Applikation der umverpackten Strohhalme an Karton-Verbundpackungen werden beispielsweise Vorrichtungen gemäß
DE 29 02 899 A1 eingesetzt. Dabei wird das Strohhalm-Endlosband von einer Vorratsrolle über Umlenkwalzen in ein getaktet angetriebenes Zuführmittel eingespeist, um das Endlosband einem Trennorgan zum Vereinzeln der Strohhalme zuzuführen und um die vereinzelten Strohhalme an ein Applikationsmittel weiterzugeben. Die umverpackten Strohhalme werden im Zuführmittel mittels eines hin und her beweglichen Schneidmessers vereinzelt und weiter in Richtung des Applikationsorts verbracht. Die gefüllten und verschlossenen Karton-Verbundpackungen werden derweil von einem Transportmittel entlang eines linearen Transportpfades mit Klebstoff versehen und einem Applikationsmittel zugeführt. Vom Applikationsmittel werden die vereinzelten Strohhalme am Applikationsort mittels eines Übertragungselements an die zugeführten Packungen appliziert. Die Taktung des Zuführmittels ermöglicht eine Vereinzelung der Strohhalme bei deren Stillstand. Dieses taktweise Vorgehen wirkt aber nicht selten limitierend auf die Verarbeitungsgeschwindigkeiten. - Das europäische Patent
EP 1 042 172 B1 schlägt eine Vorrichtung zum Anbringen von umverpackten Strohhalmen an Karton-Verbundpackungen vor, wobei das Endlosband einem sich kontinuierlich drehenden Zuführmittel zugeführt wird, wo die Vereinzelung der Strohhalme vom Endlosband durch das Zertrennen des Endlosbands mittels eines Trennmittels vollzogen wird. Das Zuführmittel speist zunächst das Endlosband ein, um dann die Strohhalme mittels eines Trennmittels in Form eines Schneidmessers zu vereinzeln. Das Schneidmesser vollführt dabei neben einer radialen Stechbewegung in Richtung der Antriebsmittel-Drehachse zusätzlich eine Mitlaufbewegung über einen gewissen Umfangsabschnitt des Zuführmittels. Die so vereinzelten Strohhalme werden an ein Applikationsmittel in Form einer sich ebenfalls kontinuierlich bewegenden Applikationsgabel weitergegeben, von der die Strohhalme an die zuvor mit Klebstoff versehenen und über ein Transportmittel entlang eines Transportpfads herangeführten Packungen angedrückt werden. Teilweise über den Umfang des Zuführmittels mitlaufende Trennmittel sind mechanisch aufwändig und relativ störungsanfällig. Oft produzieren sie auch nicht zufriedenstellende Schneidergebnisse wie abstehende Trennbrauen oder dergleichen. - Die Druckschrift
EP 0 350 590 A1 beschreibt eine Vorrichtung und ein Verfahren zum Anbringen eines verpackten Trinkhalmes an eine Packung, wobei die Packungen auf einem kontinuierlich mit einer ersten Geschwindigkeit bewegbaren Förderer transportierbar sind. Trinkhalme bewegen sich über eine erste Umlenkrolle und werden durch eine Schneidstation so bearbeitet, daß vereinzelte, verpackte Trinkhalme erzeugt werden. Die Trinkhalme werden von einem hin- und herbewegbaren Schlitten übernommen, auf eine Geschwindigkeit beschleunigt und durch einen Überführungsfinger an eine Zangenkette übergeben, welche mit gleicher Geschwindigkeit läuft. Der Mechanismus der Zangenkette bringt die Trinkhalme an Verpackungen an, welche auf Packungsförderer mit gleicher Geschwindigkeit gefördert werden. - Die Druckschrift
JP S60 172627 A - Gelöst wird die Aufgabe durch die Gegenstände der unabhängigen Ansprüche.
- Es ist Gegenstand der Erfindung, dass ein Überführmittel zum Übernehmen der vom Zuführmittel weitergegebenen Packhilfsmittel und zum Beschleunigen der übernommenen Packhilfsmittel auf eine an das Applikationsmittel angepasste Geschwindigkeit vorgesehen ist.
- Erfindungsgemäß ist vorgesehen, dass folgende Arbeitsschritte ausgeführt werden:
- Zuführen eines Packhilfsmittel-Endlosbandes zu einem Trennorgan mittels eines Zuführmittels,
- Vereinzeln der Packhilfsmittel des Packhilfsmittel-Endlosbandes am Zuführmittel mittels eines Trennorgans,
- Weitergeben der vereinzelten Packhilfsmittel mittels des Zuführmittels,
- Übernehmen und Beschleunigen der vereinzelten Packhilfsmittel auf eine an ein Applikationsmittel angepasste Geschwindigkeit durch ein Überführmittel,
- Übergeben der beschleunigten Packhilfsmittel mit an das Applikationsmittel angepasster Geschwindigkeit an das Applikationsmittel und
- Applizieren der Packhilfsmittel an durch ein Transportmittel entlang eines Packungs-Transportpfades an dem Applikationsmittel vorbeibewegten Packungen mittels des Applikationsmittels.
- Ein zwischen Zuführ- und Applikationsmittel zwischengeschaltetes Überführmittel erlaubt eine funktionale und bauliche Entkoppelung des Separierens der Packhilfsmittel vom Packhilfsmittel-Endlosband und des Applizierens der separierten Packhilfsmittel an die Packungen. So können das Vereinzeln der Packhilfsmittel und das Applizieren der Packhilfsmittel an die Packungen mit unterschiedlichen und jeweils anforderungsgemäßen Geschwindigkeiten erfolgen. Konkret heißt das, dass z. B. Schneid- und Vereinzelungsprozesse bei niedrigeren Geschwindigkeiten oder gar bei Stillstand des Packhilfsmittel-Endlosbands durchgeführt werden können, während der Applikationsprozess der vereinzelten Packhilfsmittel an die Packungen bei höheren Geschwindigkeiten durchgeführt werden kann. Derart anpassbare Geschwindigkeiten führen zu stabileren und somit zuverlässigeren Arbeitsprozessen und höheren Fertigungsqualitäten. Gleichzeitig kann der Gesamtprozess beschleunigt werden. Das Überführmittel als Überbrückungsglied ermöglicht zudem ein sicheres Verbringen der Packhilfsmittel vom Ort des Separierens an den Ort des Applizierens selbst bei höchsten Applikationsgeschwindigkeiten.
- Der Einfachheit halber kann das Überführmittel die separierten Packhilfsmittel direkt vom Zuführmittel übernehmen und/oder direkt an das Applikationsmittel übergeben. Das Zuführmittel und das Applikationsmittel sind dann unmittelbar über das Überführmittel gekoppelt, so dass weitere Baugruppen entbehrlich sind. Dies bedeutet bedarfsweise auch, dass die Packhilfsmittel an einer Stelle, der Übernahmeposition, des Übergabemittels übernommen und an einer anderen Stelle, der Übergabeposition, des Übergabemittels an das Applikationsmittel übergeben wird. Dabei erfolgt das Übernehmen und das Übergeben vorzugsweise nacheinander, insbesondere abwechselnd, um die Übernahme und die Übergabe bei unterschiedlichen Geschwindigkeiten realisieren zu können. In der Zwischenzeit kann das Überführmittel insgesamt beschleunigt oder abgebremst werden. Alternativ kann auch nur ein Teil des Überführmittels abgebremst und ein, bedarfsweise anderer, Teil des Überführmittels beschleunigt werden. Es können in diesem Falle beispielsweise Träger zur Aufnahme der Packhilfsmittel vorgesehen sein, die unabhängig voneinander abgebremst und beschleunigt werden können. Die Träger werden dann beispielsweise vor der Übernahme der Packhilfsmittel abgebremst und vor der Übergabe der Packhilfsmittel beschleunigt. Wenn das Überführmittel jeweils insgesamt beschleunigt oder abgebremst wird, kommt ein sogenannter schwelender Betrieb in Frage. Dabei kann sich das Überführmittel langsam drehen oder gar stillstehen und dabei von dem Zuführmittel ein Packhilfsmittel übernehmen. Sodann kann das Zuführmittel beschleunigt werden, um das Packhilfsmittel oder ein anderes Packhilfsmittel bei höherer Geschwindigkeit an das Applikationsmittel zu übergeben, wonach das Überführmittel wieder abgebremst wird um ein weiteres Packhilfsmittel zu übernehmen.
- Je nach der Ausgestaltung des Überführmittels können die Packhilfsmittel in horizontaler und/oder vertikaler Richtung transportiert werden.
- Verfahrensmäßig wird also zunächst dem Zuführmittel ein Packhilfsmittel-Endlosband zugeführt, das die Packhilfsmittel der Reihe nach aufweist. Das Zuführmittel führt nach der Übernahme des Packhilfsmittel-Endlosbands das Packhilfsmittel-Endlosband einem Trennorgan zu, das das Packhilfsmittel-Endlosband auftrennt und dabei die einzelnen Packhilfsmittel des Packhilfsmittel-Endlosbands separiert und vereinzelt. Die nun einzeln und separiert vorliegenden Packhilfsmittel werden von dem Zuführmittel von dem Trennorgan weg und zu einem Überführmittel hin transportiert. Das Überführmittel übernimmt die Packhilfsmittel an einer von dem Trennorgan beabstandeten Position mit einer geringen Geschwindigkeit oder bedarfsweise auch einer Geschwindigkeit von Null. Die Packhilfsmittel werden von dem Überführmittel in Richtung eines Applikationsmittels weiter transportiert, wobei die Packhilfsmittel vor der Übergabe an das Applikationsmittel beschleunigt werden, um dann mit der höheren Geschwindigkeit gegenüber der Geschwindigkeit beim Übernehmen der Packhilfsmittel vom Überführmittel an das Applikationsmittel übergeben zu werden. Diese höhere Geschwindigkeit ist abgestimmt auf die Geschwindigkeit des Applikationsmittels, das bewegt wird, um die Packhilfsmittel an Packungen zu applizieren, die über ein Transportmittel entlang eines Packungs-Transportpfads an dem Applikationsmittel vorbeibewegt werden und währenddessen die vereinzelten Packhilfsmittel empfangen.
- Der besseren Verständlichkeit halber und zur Vermeidung unnötiger Wiederholungen werden nachfolgend die Vorrichtung und das Verfahren gemeinsam beschrieben, ohne jeweils im Einzelnen zwischen der Vorrichtung und dem Verfahren zu unterscheiden. Anhand des Kontextes wird jedoch ersichtlich, welches Merkmal jeweils hinsichtlich der Vorrichtung und des Verfahrens bevorzugt ist.
- Bei einer ersten besonders bevorzugten Ausgestaltung der Vorrichtung ist das Zuführmittel zum schrittweisen Transport der Packhilfsmittel getaktet antreibbar ausgebildet. Da die einzelnen Packhilfsmittel auf dem Packhilfsmittel-Endlosband typischerweise in festen Intervallen abfolgen, ist es sinnvoll, die Zuführung ebenso in zeitlichen Intervallen vorzunehmen. So ermöglicht eine auf die Packhilfsmittel abgestimmte Arbeitstaktung die Vornahme weiterer Arbeitsprozesse. Auf diese Weise kann ein sehr genaues und reproduzierbares Zuführen der Packhilfsmittel erreicht werden. Alternativ oder zusätzlich wird so in einfacher Weise erreicht, dass das Separieren der Packhilfsmittel vom Packhilfsmittel-Endlosband erfolgen kann, während das Endlosband bzw. das Zuführmittel stillsteht oder sich nur mit geringer Geschwindigkeit bewegt.
- Wenn das Trennorgan getaktet antreibbar ausgebildet ist, lassen sich die Arbeitsschritte des Trennens und des Zuführens optimal aufeinander abstimmen. Auf diese Weise kann ein sehr genaues und reproduzierbares Trennen der Packhilfsmittel erreicht werden, das bedarfsweise erfolgen kann, während das Endlosband bzw. das Zuführmittel stillsteht oder sich nur mit geringer Geschwindigkeit bewegt. Dies führt zu einem störungsfreien Trennen und Vereinzeln der Packhilfsmittel, so dass Betriebsstörungen minimiert werden. Die Taktung des Trennorgans kann darin bestehen, dass das Trennorgan wiederholt in entgegengesetzte Richtungen hin und her bewegt wird. Die Taktung kann aber vorzugsweise auch so erfolgen, dass das Trennorgan in einer vom Packhilfsmittel-Endlosband beabstandeten Endstellung für einen kurzen Zeitraum angehalten wird. Für die Zuverlässigkeit und die Verfahrensführung ist es zudem besonders zweckmäßig, wenn das Trennorgan synchron mit dem Zuführmittel getaktet angetrieben werden kann.
- Bevorzugt ist das Zuführmittel als oder umfassend ein drehbares Karussell mit über dem Umfang verteilt angeordneten Aufnahmen für den Transport der Packhilfsmittel zum Trennorgan und zur Weitergabe der Packhilfsmittel ausgebildet. Um eine Rotationsachse drehbare Gestelle, die auch als Karusselle bezeichnet werden, ermöglichen es, über den Umfang, insbesondere gleichmäßig, verteilte Aufnahmen für die Packhilfsmittel vorzusehen. Dabei sind die Aufnahmen vorteilhafterweise korrespondierend zur Form der Packhilfsmittel ausgebildet, so dass die Aufnahmen die Packhilfsmittel formschlüssig aufnehmen und zweckmäßig halten können. Durchmesser und Teilung, d.h. die auf den Umfang bezogene Anzahl der Aufnahmen, des Karussells lassen sich so auf die Arbeitsprozesse abstimmen, dass die Leistung und Funktion der Vorrichtung verbessert werden. Des Weiteren ist aber auch der Transport der Packhilfsmittel sehr einfach und zuverlässig möglich, wobei sich bedarfsweise Bauraum einsparen lässt.
- Konstruktiv vorteilhaft sind zwischen den Aufnahmen radiale Kerben zur Aufnahme des Trennorgans beim Vereinzeln der Packhilfsmittel eingearbeitet, so dass das Trennorgan, beispielsweise in Form eines Schneidmessers, beim Vereinzelungsvorgang kurzzeitig in die Kerbe eintauchen und dabei das Packhilfsmittel-Endlosband durchtrennen kann, während vorzugsweise die angrenzenden Packhilfsmittel formschlüssig in den Aufnahmen aufgenommen sind. Auf diese Weise kann auch erreicht werden, dass das Packhilfsmittel-Endlosband eine gewisse Vorspannung aufweist, was die Vereinzelung der Packhilfsmittel vereinfacht sowie die Güte und Sicherheit der Vereinzelung verbessert.
- Das Applikationsmittel weist ein antreibbares Applikationsrad auf. Durch das Applikationsrad können die Packhilfsmittel präzise und schnell an den Applikationsort herantransportiert werden, ohne dass dazu ein erhöhter apparativer Aufwand erforderlich wäre. Dies ist in besonderem Maße der Fall, da das Applikationsrad mit im Wesentlichen konstanter Drehgeschwindigkeit antreibbar ist. Zudem wird die Zuverlässigkeit der Applikation verbessert, wenn die Umfangsgeschwindigkeit des Applikationsrads wenigstens im Wesentlichen der Transportgeschwindigkeit der Packungen entlang des Transportpfads am Ort der Applikation entspricht. So kann eine geringe Relativgeschwindigkeit zwischen den Packungen und den Packhilfsmitteln beim Applizieren derselben sichergestellt werden, so dass eine prozessstabilere Applikation mit weniger Ausschuss möglich wird. Werden zudem möglichst konstante Geschwindigkeiten gefahren, minimieren sich unerwünschte Kräfte, die aus Beschleunigungen resultieren.
- Zudem weist das Überführmittel ein mit variierenden Umfangsgeschwindigkeiten drehbares Überführrad auf. Variierende, den Gegebenheiten anpasste Geschwindigkeiten des Überführmittels verbessern die Robustheit der Prozesse, namentlich auch bei Übernahme und Übergabe der Packhilfsmittel durch das Überführmittel. Letztlich kann die Übernahme der Packhilfsmittel bei einer geeigneten Geschwindigkeit des Überführmittels und die Übergabe der Packhilfsmittel bei einer anderen geeigneten Geschwindigkeit des Überführmittels erfolgen, um beispielsweise das Gesamtverfahren zu optimieren. So sind besonders vorteilhaft das Karussell und das Überführmittel so ausgebildet, dass zur Übergabe der Packhilfsmittel vom Karussell an das Überführmittel das Karussell und das Überführmittel wenigstens annähernd stillstehen oder sich nur mit geringer Geschwindigkeit bewegen. Eine solche Konfiguration erhöht die Prozesssicherheit und vermeidet Störungen beim Übernehmen des Packhilfsmittels.
- Alternativ oder zusätzlich kann dem Transportmittel wenigstens ein Klebstoffauftragsmittel zum Beleimen der entlang des Packungs-Transportpfads dem Applikationsmittel zugeführten Packungen zugeordnet sein. Wird der Klebstoff direkt und in einem separaten Verfahrensschritt auf die Packungen aufgebracht, wird ein unerwünschtes Verkleben von Funktions- und Baugruppen verhindert und somit ein stabiler Betrieb der Vorrichtung erreicht.
- Bei einer ersten besonders bevorzugten Ausgestaltung des Verfahrens werden das Zuführmittel und das Überführmittel getaktet angetrieben. Dies bedeutet, dass das Zuführmittel und das Überführmittel jeweils gleichartige Bewegungszyklen durchlaufen. Hinsichtlich des Zuführmittels kann dieses in regelmäßigen Abständen angehalten werden, um ein Abtrennen eines weiteren Packhilfsmittels vom Packhilfsmittel-Endlosband zu bewirken. Gleiches kann für das Überführmittel gelten, wenn das Übernehmen der Packhilfsmittel durch das Überführmittel bei Stillstand des Überführmittels erfolgt. Andernfalls kann zyklisch die Geschwindigkeit des Überführmittels gesteigert und wieder reduziert werden, ohne dass es dabei zum Stillstand des Überführmittels kommt. Das Applikationsmittel bewegt sich kontinuierlich mit wenigstens im Wesentlichen konstanter Geschwindigkeit. Die Geschwindigkeit ist zudem vorzugsweise recht hoch um einen großen Durchsatz an Packungen zu ermöglichen. Dies ist einfach und zuverlässig möglich, wenn das Applikationsmittel zwischen zwei Applikationen nicht jedes Mal abgebremst und wieder beschleunigt werden muss.
- Wenn das Zuführmittel beim Vereinzeln der Packhilfsmittel mit dem Trennorgan und/oder bei der Weitergabe der Packhilfsmittel stillsteht, erfolgt vorzugsweise bei wenigstens einem Stillstand des Zuführmittels, insbesondere bei jedem Stillstand des Zuführmittels, eine Vereinzelung eines Packhilfsmittels. Wenn die Übernahme des Packhilfsmittels vom Überführmittel bei langsamer Bewegung des Zuführmittels erfolgt, kann die Weitergabe der Packhilfsmittel jeweils kurzzeitig vor oder nach dem Stillstand des Zuführmittels erfolgen, währenddessen die Geschwindigkeit des Zuführmittels ohnehin gering ist. Damit wird in jedem Fall der Betrieb vereinfacht und muss das Zuführmittel nicht so oft angehalten werden.
- Das Überführmittel kann die weitergegebenen vereinzelten Packhilfsmittel direkt oder indirekt vom Zuführmittel erhalten. Ersteres ist konstruktiv einfacher zu bewerkstelligen und kann an einer Übernahmeposition erfolgen, die für alle Packhilfsmittel identisch sein kann. Mit anderen Worten kann das Zuführmittel die vereinzelten Packhilfsmittel an das Überführmittel übergeben, wobei die Übergabe erfolgen kann, während sich das Zuführmittel und das Überführmittel bewegen, insbesondere drehen. Dabei kann das Drehen der Einfachheit der Bewegung halber als Bewegung um eine Drehachse herum angesehen werden. Das Drehen kann aber auch als sich entlang einer geschlossenen Bahn bewegen angesehen werden, wobei die Bahn kreisförmig sein kann, aber nicht sein muss.
- In einem konstruktiv und verfahrensmäßig einfachen Fall wird das Zuführmittel durch ein Karussell gebildet oder weist das Zuführmittel ein Karussell auf, das sich mit zyklisch variierender Geschwindigkeit um eine zentrale Drehachse dreht. Alternativ oder zusätzlich kann das Überführmittel als Überführrad ausgebildet sein oder ein Überführrad aufweisen. Das Überführrad dreht sich dann bevorzugt mit einer zyklisch variierenden Geschwindigkeit um eine zentrale Drehachse. Die Drehachsen sind zur Vereinheitlichung der Drehbewegungen vorzugsweise parallel zueinander ausgerichtet. Um die Weitergabe des Packhilfsmittels zuverlässig bewirken zu können, können das Karussell und das Überführrad bei der Übernahme eines Packhilfsmittels mit wenigstens im Wesentlichen derselben Umfangsgeschwindigkeit bewegt werden, so dass das Packhilfsmittel bei der Weitergabe eine wenigstens im Wesentlichen konstante Geschwindigkeit aufweist.
- Das Applikationsmittel stellt ein Applikationsrad dar oder umfasst ein Applikationsrad. So kann das Applikationsmittel problemlos mit einer konstanten Geschwindigkeit bewegt werden, indem das Applikationsrad in gleichbleibende Drehung versetzt wird. Die Drehung bzw. die Umfangsgeschwindigkeit des Applikationsrads ist dann in einfacher Weise bei der Übernahme der Packhilfsmittel und beim Applizieren der Packhilfsmittel wenigstens im Wesentlichen gleich. Die Packhilfsmittel werden also vom Applikationsrad bedarfsweise mit konstanter Geschwindigkeit vom Ort der Übernahme der Packhilfsmittel bis zum Ort der Applikation bewegt. Um dies ohne Weiteres erreichen zu können, wird das Überführrad nach dem Übernehmen eines Packhilfsmittels vom Zuführmittel auf die Umfangsgeschwindigkeit des Applikationsrads beschleunigt. Das Packhilfsmittel kann dann wenigstens im Wesentlichen ohne Geschwindigkeitsänderung vom Überführrad an das Applikationsrad weitergegeben werden.
- Ganz grundsätzlich und unabhängig von der Art des Überführmittels und des Applikationsmittels kann vorgesehen sein, die Packhilfsmittel mit einer Geschwindigkeit, insbesondere Umfangsgeschwindigkeit, vom Überführmittel an das Applikationsmittel weiterzugeben, die wenigstens im Wesentlichen der Geschwindigkeit, insbesondere Umfangsgeschwindigkeit, entspricht, mit der die Packhilfsmittel an die Packungen appliziert werden. Dies ist einfach und zuverlässig möglich.
- Die Erfindung ist nachfolgend anhand der ein Ausführungsbeispiel zeigenden Zeichnungen erläutert. Die Zeichnungen zeigen in:
- Fig. 1A-C
- eine erfindungsgemäße Vorrichtung in Draufsicht sowie ein Teil eines Packhilfsmittel-Endlosbands zur Verarbeitung mit der Vorrichtung und eine Packung mit einem von der Vorrichtung an die Packung applizierten Packhilfsmittel jeweils in seiner Seitenansicht,
- Fig. 2
- ein Zuführmittel der Vorrichtung aus
Fig. 1A umfassend ein Trennorgan in Draufsicht, - Fig. 3
- ein Detail eines Applikationsmittels der Vorrichtung aus
Fig. 1A in Draufsicht, - Fig. 4
- ein Detail der Vorrichtung aus
Fig. 1A im Bereich einer Übernahmeposition eines Überführmittels in perspektivischer Darstellung und - Fig. 5
- ein Detail der Vorrichtung aus
Fig. 1A im Bereich einer Übergabeposition eines Überführmittels in perspektivischer Darstellung. - Die
Fig. 1A zeigt eine Vorrichtung 1 zum Applizieren von Packhilfsmitteln 2 in Form von umverpackten Strohhalmen 3, an bereits gefüllte und verschlossene Packungen 4, in Form von Karton-Verbundpackungen, die vorliegend als Getränkekarton-Verbundpackungen ausgebildet sind. Die Packhilfsmittel 2 werden in Form eines Packhilfsmittel-Endlosbands 5 von einem Zuführmittel 6 in die Vorrichtung 1 eingezogen, die das Packhilfsmittel-Endlosband 5 einer Trenneinrichtung 7 zuführt. Die Trenneinrichtung 7 trennt das Packhilfsmittel-Endlosband 5 in einzelne Packhilfsmittel 2 auf, die von dem Zuführmittel 6 weiter zu einem Überführmittel 8 transportiert werden, von dem die Packhilfsmittel 2 einzeln und nacheinander übernommen werden. Diese Übernahme der Packhilfsmittel 2 erfolgt bei einer geringen Geschwindigkeit des Überführmittels 8 bzw. der Packhilfsmittel 2. An anderer Stelle werden die Packhilfsmittel 2 von dem Überführmittel 8 an ein Applikationsmittel 9 übergeben, wobei das Überführmittel 8 zwischenzeitlich beschleunigt worden ist, so dass die Übergabe der Packhilfsmittel 2 an das Applikationsmittel 9 bei deutlich höherer Geschwindigkeit erfolgt. - Das Applikationsmittel 9 appliziert die vom Überführmittel 8 an das Applikationsmittel 9 weitergegebenen Packhilfsmittel 2 in einer Applikationsposition 19 der Reihe nach an die an der Applikationsposition 19 vorbei transportierten Packungen 4. Der Transport der Packungen 4 entlang eines Packungs-Transportpfades 10 und vorbei an dem Applikationsmittel 9 erfolgt mit Hilfe eines Transportmittels 11. Dabei werden die Packungen 4 von dem Transportmittel 11 mit einer konstanten Geschwindigkeit am Applikationsmittel 9, insbesondere an der Applikationsposition 19, vorbei transportiert. Das dargestellte und insoweit bevorzugte Transportmittel 11 weist dazu einen mit Nocken 13 versehenen Transportriemen 14 auf, der sich in der Transportrichtung der Packungen 4 erstreckt. Die einzelnen Nocken 13 sind formschlüssig mit den Packungen 4 in Eingriff und verschieben die Packungen 4 in definierten Abständen und definierter Geschwindigkeit entlang des Applikationsmittels 9.
- Das Applikationsmittel 9 ist bei der dargestellten und insoweit bevorzugten Ausgestaltung als ein Applikationsrad 1 ausgeführt, das mehrere um die Drehachse 16 des Applikationsrad 15 rotierende und gleichmäßig über den Umfang des Applikationsrads 15 verteilt angeordnete Applikatoren 17 aufweist. Die Applikatoren 17 übernehmen an einer Übergabeposition 18 jeweils ein Packhilfsmittel 2 und verbringen dieses zur Applikationsposition 19, um es dort an eine vorbeitransportierte Packung 4 zu applizieren.
- Die Verbindung zwischen Packhilfsmittel 2 und Packung 4 ist in dem dargestellten Ausführungsbeispiel durch eine Klebeverbindung gegeben, wobei auch andere Verbindungen denkbar sind. Als Klebstoff wird Heißleim eingesetzt, der durch am ein Packungs-Transportpfad 10 angeordnetes Klebstoffauftragsmittel 20, insbesondere in Form von Klebstoffauftragsdüsen, punktuell an die Seiten 12 der Packungen 4 aufgebracht wird. An der Applikationsposition 19 wird jeweils ein Packhilfsmittel 2 in die Heißleimpunkte gedrückt. Um die so applizierten Packhilfsmittel 2 in Position zu halten und dem Heißleim eine gewisse Abbindzeit zu gewähren, drückt ein Andrückriemen 22 unmittelbar ab der Applikationsposition 19 über eine gewisse Wegstrecke die frisch applizierten Packhilfsmittel 2 gegen die Packungen 4, während die Packungen 4 weitertransportiert werden.
- Die Packhilfsmittel 2 werden der Vorrichtung 1 in Form eines Packhilfsmittel-Endlosbands 5 zugeführt, das teilweise in der
Fig. 1B näher dargestellt ist, und nach einer Vereinzelung an Packungen 4 appliziert. Die Packhilfsmittel 2 setzen sich aus einem Strohhalm 3 und zwei Folien 23 zusammen. Als Strohhalme 3 kommen dabei verschiedene Formen in Frage, insbesondere handelt es sich jedoch um wenigstens teilweise U-förmige oder I-förmige Strohhalme 3. Das dargestellte und insoweit bevorzugte Packhilfsmittel-Endlosband 5 umfasst U-förmige Strohhalme 3. Die Folien 23 sind an ihren Rändern 24 verschweißt und bilden dazwischen eine Tasche 25, in der der Strohhalm 3 aufgenommen ist. Mit anderen Worten ist der Strohhalm 3 in Folie 23 umverpackt. Das Packhilfsmittel-Endlosband 5 wird durch eine Aneinanderreihung der Packhilfsmittel 2 gebildet, wobei jeweils die Folien benachbarter Packhilfsmittel 2 miteinander verbunden sind. Beim dargestellten und insoweit bevorzugten Packhilfsmittel-Endlosband 5 sind die Strohhalme 3 zwischen zwei sich entlang des gesamten Packhilfsmittel-Endlosbands 5 erstreckenden Folien aufgenommen. Anders ausgedrückt stellt das Packhilfsmittel-Endlosband 5 eine "endlose" Abfolge von Packhilfsmitteleinheiten dar. Eine Packung 4 mit einem daran applizierten und vom Packhilfsmittel-Endlosband 5 separierten Packhilfsmittel 2 ist in derFig. 1C beispielhaft dargestellt. Das Packhilfsmittel 2 ist etwa diagonal zur zugeordneten Seite 12 der Packung 4 appliziert, was jedoch nicht zwingend der Fall sein muss. - Die dargestellten und insoweit bevorzugten Packungen 4 weisen ein fließfähiges Lebensmittel, insbesondere ein Getränk auf. Zudem handelt es sich bei der Packung 4 um eine Karton-Verbundpackung, mithin eine Getränkekarton-Verbundpackung. Die Verpackung ist aus einem Packungslaminat gebildet, das Schichten aus unterschiedlichen Packstoffen, nämlich wenigstens Karton und Kunststoff umfasst. Die Kunststoffschichten sind an den Außenseiten des Packungslaminats vorgesehen und durch thermoplastische Kunststoffe, insbesondere Polyethylen (PE), gebildet. Durch Falten und Siegeln des Packungslaminats ist die Packung 4 geformt und verschlossen. Bedarfsweise ist das Packungslaminat einseitig mit einem Dekor bedruckt.
- In der
Fig. 2 ist ein das Zuführmittel 6 umfassendes Detail der Vorrichtung 1 aus derFig. 1A dargestellt. Das Zuführmittel 6 umfasst ein sich um eine zentrale Drehachse 26 im Uhrzeigersinn drehendes Karussell 27, das über seinen Umfang verteilt Aufnahmen 28 zur teilweisen Aufnahme 28 der Packhilfsmittel 2 aufweist. Die Aufnahmen 28 sind den Formen der Strohhalme 3 nachgebildet, so dass die Strohhalme 3 und damit die Packhilfsmittel 2 formschlüssig in den Aufnahmen 28 gehalten sind. Damit die Packhilfsmittel 2 in den Aufnahmen 28 verbleiben, ist umfangsseitig eine ortsfeste Seitenwand 21 vorgesehen. Im Bereich des Einzugs des Packhilfsmittel-Endlosbandes 5 vom Zuführmittel 6 ist ein torsionsfederbelastetes Spannblech 30 vorgesehen, das das Packhilfsmittel-Endlosband 5 umfangsseitig führt und gegen das Karussell 27 und in die Aufnahmen 28 drückt. Das Spannblech 30 geht in Transportrichtung des Packhilfsmittel-Endlosbands 5 gesehen in die Seitenwand 21 über. Soll ein neues Packhilfsmittel-Endlosband 5 eingelegt werden, kann das Spannblech 30 nach außen geschwenkt und arretiert werden, um das Einlegen des Packhilfsmittel-Endlosbands 5 zu vereinfachen. Das dargestellte und insoweit bevorzugte Zuführmittel 6 wird durch das Karussell 27 mit den Aufnahmen 28, der Seitenwand 21 und dem Spannblech 30 gebildet. - Dem Zuführmittel 6 zugeordnet ist eine Trenneinrichtung 7 zur Vereinzelung der Packhilfsmittel 2 vom Packhilfsmittel-Endlosband 5 mit einem Trennorgan 31. Das Trennorgan 31 wird bei der dargestellten und insoweit bevorzugten Vorrichtung 1 mit einem Antriebsmechanismus 32 radial wenigstens im Wesentlichen in Richtung der Drehachse 26 des Karussells 27 hin und her bewegt, wie dies durch den Doppelpfeil angedeutet ist. Das Trennorgan 31 ist an der dem Packhilfsmittel-Endlosband 5 zugeordneten Kante 33 als geschärftes Schneidmesser ausgeführt und durchschneidet das Packhilfsmittel-Endlosband 5 im Verbindungsbereich zweier aufeinanderfolgender Packhilfsmittel 2, wodurch die Packhilfsmittel 2 des Packhilfsmittel-Endlosbands 5 nacheinander voneinander separiert bzw. vereinzelt werden. Dabei greift das Trennorgan 31 wenigstens teilweise in entlang des Umfangs des Karussells 27 zwischen den Aufnahmen 28 für die Packhilfsmittel 2 angeordnete Kerben 34 ein.
- Das Karussell 27 arbeitet in einem getakteten Betrieb, in dem das Karussell 27 taktweise angehalten und um ein Umfangssegment weitergedreht wird, das der Breite eines Packhilfsmittels 2 entspricht. Dazu ist das Karussell 27 mit dem Antriebsmechanismus 32 der Trenneinrichtung 7 so synchronisiert, dass bei Stillstand des Karussells 27 das Trennorgan 31 in Richtung der Drehachse 26 des Karussells 27 nach vorne und wieder zurück in die Ausgangsstellung bewegt wird. Beim Verstellen des Trennorgans 31 nach vorne durchtrennt das Trennorgan 31 das Packhilfsmittel-Endlosband 5 im Bereich der zugeordneten Kerbe 34. Sobald das Trennorgan 31 wieder außer Eingriff mit der Kerbe 34, insbesondere wieder in der Ausgangsstellung angekommen, ist, dreht das Karussell 27 in einem weiteren Takt zur nächsten Position weiter, wodurch das Trennorgan 31 der nächsten Kerbe 34 gegenübersteht und durch ein Verstellen nach vorne das nächste Packhilfsmittel 2 vom Packhilfsmittel-Endlosband 5 abtrennen kann. Die Trenneinrichtung 7 ist ortsfest am Zuführmittel 6 angeordnet und nur das Trennorgan 31 bewegt sich hin und her, und zwar in einer linearen und bezogen auf das Karussell 27 radialen Bewegung. Ein taktweises Verstellen des Trennorgans 31 in Umfangsrichtung erfolgt beim dargestellten und insoweit bevorzugten Trennorgan 31 nicht.
- Um kleinere Schneidrückstände, wie etwa Schneidbrauen, aufnehmen und/oder abführen zu können, bzw. eine ausreichende Ent- und/oder Belüftung bereitzustellen, enden die Kerben 34 in radialer Richtung in sich vertikal erstreckenden Entleerungskanälen 35, die einen Querschnitt aufweisen, welcher größer ist als die Breite der Kerben 34 angrenzend zu den Entleerungskanälen 35. Die auf die beschriebene Weise vereinzelten Packhilfsmittel 2 werden mit jedem weiteren Takt des Zuführmittels 6 weiter in Richtung einer Übernahmeposition 36 weitertransportiert, von der aus die Packhilfsmittel 2 an das Überführmittel 8 übergeben und von dem Überführmittel 8 übernommen werden.
- In der
Fig. 3 ist ein Detail des Applikationsmittels 9 umfassend einen Applikator 17 dargestellt. Der äußere Teil des Applikators 17, der das Packhilfsmittel 2 von der Übergabeposition 18 in die Applikationsposition 19 bewegt, weist einen Applikationsfinger 37 und einen Führungsfinger 38 auf. Der Applikationsfinger 37 weist stirnseitig zwei Kehlen 39 auf, die mit der Form des Packhilfsmittels 2, insbesondere des Strohhalms 3, korrespondieren. Die beiden Kehlen 39 werden zum Halten der beiden Schenkel 40 des U-förmigen Strohhalms 3 genutzt, wie dies durch ein strichliniert eingezeichnetes Packungshilfsmittel mitsamt einem Strohhalm 3 dargestellt ist. Bei Verwendung von geradlinigen, also I-förmigen, Strohhalmen 3 wäre grundsätzlich eine Kehle 39 ausreichend. Der Applikationsfinger 37 ist geringfügig gegen die Federkraft einer Feder 41 verschwenkbar und so konfiguriert, dass das Packhilfsmittel 2 zwischen der Übergabeposition 18 und der Applikationsposition 19 zwischen Applikationsfinger 37, Führungsfinger 38 und einer umfangsseitig des Applikationsrads 15 vorgesehenen Seitenbande 42 eingespannt und somit sicher geführt. Der Führungsfinger 38 verhindert dabei, dass das Packhilfsmittel 2 in Umfangsrichtung außer Eingriff mit dem Applikationsfinger 37 gerät. - Kurz vor der Applikationsposition 19 endet die Seitenbande 42, wie dies in der
Fig. 1A dargestellt ist, so dass das Packhilfsmittel 2 durch die Federkraft der Feder 41 in den Heißleim der vorbeibewegten Packung 4 gedrückt wird. Das dargestellte Applikationsrad 15 verfügt zudem über einen - hier nicht näher beschriebenen - Verstellmechanismus, der es erlaubt, die Packhilfsmittel 2 zwischen der Übergabeposition 18 und der Applikationsposition 19 derart um eine radiale Achse zu schwenken, dass die Packhilfsmittel 2 in der Übergabeposition 18 parallel zur Drehachse 16 des Applikationsrads 15 übernommen und diagonal zu der zugeordneten Seite 12 der zugeordneten Packung 4 appliziert werden können, wie dies in derFig. 1C dargestellt ist. - Das Applikationsrad 15 dreht im gezeigten und insofern bevorzugten Ausführungsbeispiel mit einer derart konstanten Winkelgeschwindigkeit bzw. Umfangsgeschwindigkeit, dass die Packhilfsmittel 2 bzw. die Applikatoren 17 stirnseitig an der Applikationsposition 19 eine Umfangsgeschwindigkeit aufweisen, die in Betrag und Richtung zumindest annähernd der Geschwindigkeit der Packungen 4 an der Applikationsposition 19 entsprechen. Ein solcher Betrieb minimiert Relativgeschwindigkeiten zwischen Packung 4 und Packhilfsmittel 2 beim Applizieren.
- Zwischen Applikationsmittel 9 und Zuführmittel 6 ist ein Überführmittel 8 mit einem um eine Drehachse 43 drehbaren Überführrad 44 und einer weiteren, umfangsseitig vorgesehenen Seitenwand 29 vorgesehen, wie dies im Detail in der
Fig. 4 dargestellt ist. Das Überführrad 44 weist längliche Aufnahmenuten 45 für die Aufnahme der Packhilfsmittel 2 auf, die gleichmäßig über den Umfang des Überführrads 44 verteilt angeordnet sind. Der besseren Übersichtlichkeit halber sind die Packhilfsmittel 2 jedoch ebenso wie das Packhilfsmittel-Endlosband 5 nicht dargestellt. Die Packhilfsmittel 2 sind zwischen dem Überführrad 44 und der ortsfesten weiteren Seitenwand 29 geführt und werden durch den Formschluss zwischen den Aufnahmenuten 45 und den Packhilfsmitteln 2 in Umfangsrichtung transportiert. In der Übernahmeposition 36 übernimmt das Überführmittel 8 das weitergegebene Packhilfsmittel 2 vom Karussell 27 und beschleunigt das Packhilfsmittel 2 zwischen Übernahmeposition 36 und der Übergabeposition 18 auf eine dem Applikationsrad 15 angepasste Geschwindigkeit und übergibt das Packhilfsmittel 2 an der Übergabeposition 18 einem Applikator 17 des Applikationsrads 15. - Neben dem Zuführmittel 6 ist der Teil des Überführmittels 8 dargestellt, der sich im Bereich der Übernahmeposition 36 des Packhilfsmittels 2 vom Karussell 27 auf das Überführrad 44 des Überführmittels 8 befindet. Das Karussell 27 ist durch eine Vielzahl gestapelter und zueinander beabstandeter Plattenelemente 46 gebildet ist, so dass sich mehrere Zwischenebenen 47 zwischen den Plattenelementen 34 ausbilden. In diese Zwischenebenen 35 ragen als Fortsätze der weiteren Seitenwand 21 mehrere ortsfeste Auskämmlamellen 48. Die Auskämmlamellen 48 bilden in ihrer Summe eine abschnittsweise Führung beim Herausführen der Packhilfsmittel 2 aus den Aufnahmen 28 des Karussells 27, so dass mit der weiteren Seitenwand 21 dem Packhilfsmittel 2 eine lückenlose Führung beim Übernehmen des Packhilfsmittels 2 in die Aufnahmenuten 45 des Überführrads 44 aus den Aufnahmen 2 des Karussells 27 geboten ist.
- Bei der Übergabe der Packhilfsmittel 2 weist das Überführrad 44 im Bereich der Aufnahmenuten 45 eine etwa gleichgroße, wenn auch geringe, Umfangsgeschwindigkeit wie das Karussell 27 im Bereich der Aufnahmen 28 auf, so dass die Packhilfsmittel 2 wenigstens im Wesentlichen beschleunigungsfrei vom Zuführmittel 6 auf das Überführmittel 8 weitergegeben werden können. Das Überführrad 44 wird weiter verdreht und insbesondere ab dem Zeitpunkt beschleunigt, ab dem das Packhilfsmittel 2 zwischen Überführrad 44 und der weiteren Seitenwand 29 aufgenommen und geführt ist.
- In der
Fig. 5 , in der der besseren Übersichtlichkeit halber ebenfalls die Packhilfsmittel 2 nicht dargestellt sind, sind das Überführmittel 8 und das Applikationsmittel 9 im Bereich der Übergabeposition 18 dargestellt. Das Überführrad 44 ist in ähnlicher Weise wie das Karussell 27 aufgebaut, nämlich aus mehreren Plattenelementen 46, die ihrerseits ebenfalls Zwischenebenen 47 bilden, in die mehrere Auskämmlamellen 49 als Fortführung der Seitenbande 42 ragen. Dies ermöglicht das Auskämmen der Packhilfsmittel 2 aus den Aufnahmenuten 45 des Überführrads 44 im Bereich der Übergabeposition 18. - Beim Übergeben des Packhilfsmittels 2 vom Überführmittel 8 auf das Applikationsmittel 9 weisen das Überführrad 44 und das Applikatorrad 15 wenigstens annähernd die gleichen Umfangsgeschwindigkeiten auf. Nach dem Übergeben wird das Packhilfsmittel 2 vom Applikationsfinger 37 und vom Führungsfinger 38 gehalten. Beim weiteren Drehen des Applikatorrads wird das Packhilfsmittel 2 durch die Auskämmlamellen 49 vollständig aus der Aufnahmenut 45 ausgekämmt und wird das Packhilfsmittel 2 beim weiteren Drehen durch die Seitenbande 42 geführt und an die Seitenbande 42 gedrückt. Die Packhilfsmittel 2 werden von dem Applikatorrad 15 von der Übergabeposition 18 bis in die Applikationsposition 19 mit einer konstanten Geschwindigkeit transportiert und dabei um eine radiale Achse geschwenkt. In der Applikationsposition 19 wird das Packhilfsmittel 2 dann schräg an die vorbeitransportierte Packung 4 appliziert.
-
- 1
- Vorrichtung
- 2
- Packhilfsmittel
- 3
- Strohhalme
- 4
- Packungen
- 5
- Packhilfsmittel-Endlosband
- 6
- Zuführmittel
- 7
- Trenneinrichtung
- 8
- Überführmittel
- 9
- Applikationsmittel
- 10
- Packungs-Transportpfad
- 11
- Transportmittel
- 12
- Seite der Packung
- 13
- Nocken
- 14
- Transportriemen
- 15
- Applikationsrad
- 16
- Drehachse
- 17
- Applikator
- 18
- Übergabeposition
- 19
- Applikationsposition
- 20
- Klebstoffauftragsmittel
- 21
- Seitenwand
- 22
- Andrückriemen
- 23
- Folie
- 24
- Rand
- 25
- Tasche
- 26
- Drehachse
- 27
- Karussell
- 28
- Aufnahmen
- 29
- Seitenwand
- 30
- Spannblech
- 31
- Trennorgan
- 32
- Antriebsmechanismus
- 33
- Kante
- 34
- Kerbe
- 35
- Entleerungskanal
- 36
- Übernahmeposition
- 37
- Applikationsfinger
- 38
- Führungsfinger
- 39
- Kehle
- 40
- Schenkel
- 41
- Feder
- 42
- Seitenbande
- 43
- Drehachse
- 44
- Überführrad
- 45
- Aufnahmenut
- 46
- Plattenelement
- 47
- Zwischenebene
- 48
- Auskämmlamelle
- 49
- Auskämmlamelle
Claims (13)
- Vorrichtung (1) zum separaten Applizieren von als Packhilfsmittel-Endlosband (5) zugeführten Packhilfsmitteln (2), vorzugsweise umverpackten Strohhalmen (3), an Packungen (4), insbesondere Karton-Verbundpackungen, mit einem Trennorgan (31) zum Vereinzeln der Packhilfsmittel (2) des Packhilfsmittel-Endlosbandes (5), einem Zuführmittel (6) zum Zuführen des Packhilfsmittel-Endlosbandes (5) zum Trennorgan (31) und zum Weitergeben der durch das Trennorgan (31) vereinzelten Packhilfsmittel (2), einem Applikationsmittel (9) zum Applizieren der vereinzelten Packhilfsmittel (2) an die Packungen (4) und einem Transportmittel (11) zum Transportieren der Packungen (4) entlang eines Packungs-Transportpfads (10) zum Applikationsmittel (9), wobei ein Überführmittel (8) zum Übernehmen der vom Zuführmittel (6) weitergegebenen Packhilfsmittel (2) und zum Beschleunigen der übernommenen Packhilfsmittel (2) auf eine an das Applikationsmittel (9) angepasste Geschwindigkeit vorgesehen ist,
dadurch gekennzeichnet, dass
das Applikationsmittel (9) ein mit im Wesentlichen konstanter Drehgeschwindigkeit antreibbares Applikationsrad (15) aufweist und dass das Überführmittel (8) ein mit variierenden Umfangsgeschwindigkeiten drehbares Überführrad (44) aufweist, dessen Umfangsgeschwindigkeit auf eine an das Applikationsmittel (9) angepasste Geschwindigkeit beschleunigt wird, um die vom Überführmittel (8) übernommenen Packhilfsmittel (2) zu beschleunigen. - Vorrichtung nach Anspruch 1,
dadurch gekennzeichnet, dass
das Zuführmittel (6) zum schrittweisen Transport der Packhilfsmittel (2) getaktet antreibbar ausgebildet ist. - Vorrichtung nach einem der Ansprüche 1 oder 2,
dadurch gekennzeichnet, dass
das Trennorgan (31) getaktet, insbesondere synchron mit dem Zuführmittel (6), antreibbar ausgebildet ist. - Vorrichtung nach einem der Ansprüche 1 bis 3,
dadurch gekennzeichnet, dass
das Zuführmittel (6) ein drehbares Karussell (27) mit über dem Umfang verteilt angeordneten Aufnahmen (28) für den Transport der Packhilfsmittel (2) zum Trennorgan (7) und zur Weitergabe der Packhilfsmittel (2) aufweist. - Vorrichtung nach Anspruch 4,
dadurch gekennzeichnet, dass zwischen den Aufnahmen (28) radiale Kerben (34) zur Aufnahme des Trennorgans (31) beim Vereinzeln eingearbeitet sind. - Vorrichtung nach einem der Ansprüche 1 bis 5,
dadurch gekennzeichnet, dass
das Applikationsmittel (9) ein mit einer im Wesentlichen der Transportgeschwindigkeit der Packungen (4) entsprechenden Umfangsgeschwindigkeit antreibbares Applikationsrad (15) aufweist. - Vorrichtung nach einem der Ansprüche 1 bis 6,
dadurch gekennzeichnet, dass
das Zuführmittel (6), insbesondere ein Karussell (27) des Zuführmittels (6), und das Überführmittel (8), insbesondere ein Überführrad (44) des Überführmittels (8), zur Übernahme der Packhilfsmittel (2) vom Zuführmittel (6) auf das Überführmittel (8) bei wenigstens annähernd gleicher Geschwindigkeit von Zuführmittel (6) und Überführmittel (8) an einer Übernahmeposition (36) ausgebildet sind. - Vorrichtung nach einem der Ansprüche 1 bis 7,
dadurch gekennzeichnet, dass dem Transportmittel (11) wenigstens ein Klebstoffauftragsmittel (20) zum Beleimen der entlang des Packungs-Transportpfads (10) dem Applikationsmittel (9) zugeführten Packungen (4) zugeordnet ist. - Verfahren zum separaten Applizieren von in einem Packhilfsmittel-Endlosband (5) zugeführten Packhilfsmitteln (2), vorzugsweise umverpackten Strohhalmen (3), an Packungen (4), insbesondere Karton-Verbundpackungen, vorzugsweise mit einer Vorrichtung nach einem der Ansprüche 1 bis 8, gekennzeichnet durch die Schritte- Antreiben eines Applikationsmittels (9) kontinuierlich und mit wenigstens im Wesentlichen konstanter Geschwindigkeit, wobei das Applikationsmittel (9) ein sich mit wenigstens im Wesentlichen konstanter Geschwindigkeit drehendes Applikationsrad (15) zum Übernehmen und Applizieren der Packhilfsmittel (2) aufweist,- Zuführen eines Packhilfsmittel-Endlosbandes (5) zu einem Trennorgan (31) mittels eines Zuführmittels (6),- Vereinzeln der Packhilfsmittel (2) des Packhilfsmittel-Endlosbandes (5) am Zuführmittel (6) mittels eines Trennorgans (31),- Weitergeben der vereinzelten Packhilfsmittel (2) mittels des Zuführmittels (6),- Übernehmen und Beschleunigen der vereinzelten Packhilfsmittel (2) auf eine an ein Applikationsmittel (9) angepasste Geschwindigkeit durch ein Überführmittel (8) in Form eines mit variierenden Umfangsgeschwindigkeiten drehbaren Überführrads (44), dessen Umfangsgeschwindigkeit auf eine an das Applikationsmittel (9) angepasste Geschwindigkeit beschleunigt wird, um die vom Überführmittel (8) übernommenen Packhilfsmittel (2) zu beschleunigen, wobei die Packhilfsmittel (2) mit dem Überführmittel (8) bis zum Übergeben der Packhilfsmittel (2) an das Applikationsmittel (9) wenigstens im Wesentlichen auf die Umfangsgeschwindigkeit des Applikationsmittels (9) beschleunigt werden,- Übergeben der beschleunigten Packhilfsmittel (2) mit an das Applikationsmittel (9) angepasster Geschwindigkeit an das Applikationsmittel (9) und- Applizieren der Packhilfsmittel (2) an durch ein Transportmittel (11) entlang eines Packungs-Transportpfades (10) an dem Applikationsmittel (9) vorbeibewegten Packungen (4) mittels des Applikationsmittels (9).
- Verfahren nach Anspruch 9,
dadurch gekennzeichnet, dass
das Zuführmittel (6) und das Überführmittel (8) getaktet angetrieben werden. - Verfahren nach Anspruch 9 oder 10,
dadurch gekennzeichnet, dass
das Zuführmittel (6) beim Vereinzeln der Packhilfsmittel (2) mit dem Trennorgan (31) und/oder bei der Weitergabe der Packhilfsmittel (2) stillsteht. - Verfahren nach einem der Ansprüche 9 bis 11,
dadurch gekennzeichnet, dass
das Überführmittel (8) die vereinzelten Packhilfsmittel (2), vorzugsweise direkt, an einer Übernahmeposition (36) vom Zuführmittel (6) übernimmt und/oder, vorzugsweise direkt, an einer Übergabeposition (18) an das Applikationsmittel (9) übergibt und/oder dass die Packhilfsmittel (2) von einem Karussell (27) des Zuführmittels (6) an ein Überführrad (44) des Übergabemittels (8), insbesondere durch Drehen des Karussells (27) und des Überführrads (44), und/oder von dem Überführrad (44) des Übergabemittels (8) an ein Applikationsrad (15) des Applikationsmittels (9), insbesondere durch Drehen des Überführrads (44) und des Applikationsrads (15), weitergeben wird. - Verfahren nach einem der Ansprüche 9 bis 12,
dadurch gekennzeichnet, dass die Packhilfsmittel (2) mit einer Geschwindigkeit, insbesondere Umfangsgeschwindigkeit, vom Überführmittel (8) an das Applikationsmittel (9) übergeben werden, die wenigstens im Wesentlichen der Geschwindigkeit, insbesondere Umfangsgeschwindigkeit, entspricht, mit der die Packhilfsmittel (2) an die Packung (4) appliziert werden.
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP17020177.6A EP3395703B8 (de) | 2017-04-27 | 2017-04-27 | Verfahren und vorrichtung zum applizieren von packhilfsmitteln |
| CN201880027712.9A CN110914162B (zh) | 2017-04-27 | 2018-04-23 | 用于施加包装辅助件的方法和设备 |
| US16/607,383 US11273945B2 (en) | 2017-04-27 | 2018-04-23 | Method and device for applying additive packaging material |
| PCT/EP2018/060331 WO2018197407A1 (de) | 2017-04-27 | 2018-04-23 | Verfahren und vorrichtung zum applizieren von packhilfsmitteln |
| JP2019558506A JP7165678B2 (ja) | 2017-04-27 | 2018-04-23 | 付加的包装材料を貼着するための方法およびデバイス |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP17020177.6A EP3395703B8 (de) | 2017-04-27 | 2017-04-27 | Verfahren und vorrichtung zum applizieren von packhilfsmitteln |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP3395703A1 EP3395703A1 (de) | 2018-10-31 |
| EP3395703B1 true EP3395703B1 (de) | 2022-09-14 |
| EP3395703B8 EP3395703B8 (de) | 2022-10-19 |
Family
ID=58668705
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP17020177.6A Active EP3395703B8 (de) | 2017-04-27 | 2017-04-27 | Verfahren und vorrichtung zum applizieren von packhilfsmitteln |
Country Status (1)
| Country | Link |
|---|---|
| EP (1) | EP3395703B8 (de) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114291363A (zh) * | 2022-01-24 | 2022-04-08 | 东莞市村本自动化设备有限公司 | 一种多功能玻璃叠纸机 |
| CN117944951B (zh) * | 2024-03-26 | 2024-05-28 | 云南大联塑料制品有限公司 | 一种具有精准下料功能的塑料吸管包装设备 |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS60172627A (ja) * | 1984-02-17 | 1985-09-06 | トキワ工業株式会社 | ストロ−包装体等の容器への貼着装置 |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| SE424847B (sv) | 1978-01-30 | 1982-08-16 | Tetra Pak Int | Maskin for applicering av sugror pa forpackningsbehallare |
| DE3824013C2 (de) * | 1988-07-15 | 1997-02-13 | Profor Ab | Verfahren zum Anbringen eines verpackten Trinkhalmes an einer Packung und Vorrichtung für dieses Anbringen |
| DE4114191C1 (en) * | 1991-05-01 | 1992-04-23 | Ostma Maschinenbau Gmbh, 5352 Zuelpich, De | Application of long strip of material - involves conveyor belt and associated pressure and counter-pressure belts |
| SE509833C2 (sv) | 1997-05-16 | 1999-03-15 | Tetra Laval Holdings & Finance | Anordning för applicering av sugrör |
-
2017
- 2017-04-27 EP EP17020177.6A patent/EP3395703B8/de active Active
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS60172627A (ja) * | 1984-02-17 | 1985-09-06 | トキワ工業株式会社 | ストロ−包装体等の容器への貼着装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP3395703A1 (de) | 2018-10-31 |
| EP3395703B8 (de) | 2022-10-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2906473B1 (de) | Hochleistungs-verpackungsverfahren zur verpackung von, insbesondere kleinstückigen, produkten und hochleistungs-verpackungseinrichtung, insbesondere zur durchführung des verfahrens | |
| EP2785598B1 (de) | Vorrichtung zur bildung von verpackungseinheiten | |
| EP2477907A1 (de) | Packungen insbesondere für zigaretten sowie verfahren und vorrichtung zum herstellen derselben | |
| DE4446104A1 (de) | Verfahren und Vorrichtung zum Herstellen eines Getränkebehälters | |
| WO2013113464A1 (de) | Ovale behälterbehandlungsvorrichtung | |
| DE102015001027A1 (de) | Verfahren und Vorrichtung zum Herstellen von Zigarettenpackungen | |
| EP4402066A1 (de) | Verfahren und vorrichtung zum herstellen von packungen für produkte der zigarettenindustrie | |
| EP3395730A1 (de) | Bearbeitungsvorrichtung und verfahren zum bearbeiten von vereinzelten packungen | |
| WO2018050376A1 (de) | Vorrichtung und verfahren zur herstellung von gebinden mit tragegriffen | |
| WO2018197407A1 (de) | Verfahren und vorrichtung zum applizieren von packhilfsmitteln | |
| EP3459865B1 (de) | Verfahren und vorrichtung zum stapelförmigen verpacken von kleinstückigen produkten | |
| EP3395703A1 (de) | Verfahren und vorrichtung zum applizieren von packhilfsmitteln | |
| EP3615435B1 (de) | Applikationsvorrichtung, applikationseinrichtung und verfahren zum applizieren von zusatzelementen an packungen | |
| DE102017109126A1 (de) | Bearbeitungsvorrichtung und Verfahren zum Bearbeiten von vereinzelten Packungen | |
| EP3707076A1 (de) | Verfahren zum bearbeiten und/oder füllen von verpackungen | |
| DE102012014951B3 (de) | Verfahren und Vorrichtung zum Verpacken von portionierten, im Verarbeitungszustand flüssigen oder pastösen Produkten | |
| DE102017109121A1 (de) | Verfahren und Vorrichtung zum Applizieren von Packhilfsmitteln | |
| EP3350098A1 (de) | Verfahren und vorrichtung zum herstellen von packungen für zigaretten | |
| EP0872421B1 (de) | Schneid- und Übergabestation einer getaktet arbeitenden Flachbeutelmaschine | |
| WO2018197409A1 (de) | Bearbeitungsvorrichtung und verfahren zum bearbeiten von vereinzelten packungen | |
| EP3436361A1 (de) | Verfahren und vorrichtung zum bilden von behältniszusammenstellungen | |
| DE102019134111A1 (de) | Vereinzelungsvorrichtung und Verfahren zum Vereinzeln von Packungen und Bearbeitungsvorrichtung zum Bearbeiten von Verpackungen | |
| DE2545739A1 (de) | Verfahren zur herstellung von verpackungen und maschine zur durchfuehrung des verfahrens | |
| EP3615434A1 (de) | Applikationsvorrichtung zum applizieren von zusatzelementen an packungen | |
| WO2021058113A1 (de) | Quersiegelvorrichtung für eine schlauchbeutelverpackungsmaschine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20190424 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17Q | First examination report despatched |
Effective date: 20190917 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20211112 |
|
| GRAJ | Information related to disapproval of communication of intention to grant by the applicant or resumption of examination proceedings by the epo deleted |
Free format text: ORIGINAL CODE: EPIDOSDIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTC | Intention to grant announced (deleted) | ||
| INTG | Intention to grant announced |
Effective date: 20220330 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502017013787 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PK Free format text: BERICHTIGUNG B8 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1518569 Country of ref document: AT Kind code of ref document: T Effective date: 20221015 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 502017013787 Country of ref document: DE Owner name: SIG COMBIBLOC SERVICES AG, CH Free format text: FORMER OWNER: SIG TECHNOLOGY AG, NEUHAUSEN AM RHEINFALL, CH Ref country code: DE Ref legal event code: R081 Ref document number: 502017013787 Country of ref document: DE Owner name: SIG SERVICES AG, CH Free format text: FORMER OWNER: SIG TECHNOLOGY AG, NEUHAUSEN AM RHEINFALL, CH |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: SIG COMBIBLOC SERVICES AG |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20220914 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20221214 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20221215 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230116 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20230114 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502017013787 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| 26N | No opposition filed |
Effective date: 20230615 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230427 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20230430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230430 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230430 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230427 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 1518569 Country of ref document: AT Kind code of ref document: T Effective date: 20230427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 502017013787 Country of ref document: DE Owner name: SIG SERVICES AG, CH Free format text: FORMER OWNER: SIG COMBIBLOC SERVICES AG, NEUHAUSEN AM RHEINFALL, CH |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250417 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250430 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250422 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20170427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20170427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220914 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20260324 Year of fee payment: 10 |