EP0930144B1 - Spritzgiessmaschine - Google Patents
Spritzgiessmaschine Download PDFInfo
- Publication number
- EP0930144B1 EP0930144B1 EP99250004A EP99250004A EP0930144B1 EP 0930144 B1 EP0930144 B1 EP 0930144B1 EP 99250004 A EP99250004 A EP 99250004A EP 99250004 A EP99250004 A EP 99250004A EP 0930144 B1 EP0930144 B1 EP 0930144B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- injection moulding
- conveying unit
- vibrating element
- moulding machine
- material conveying
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/46—Means for plasticising or homogenising the moulding material or forcing it into the mould
- B29C45/58—Details
- B29C45/585—Vibration means for the injection unit or parts thereof
Definitions
- the invention relates to an injection molding machine according to the preamble of Claims 1 and 2.
- DE-Gbm 91 06 039 is a gum massage brush with a handle known in which the final finished shape of the brush by folding on two Folding axes by locally softening known plastics, e.g. by Ultrasound.
- the subject of this known utility model is thus the finished one Component, but not the plastic mass in the injection molding machine, by ultrasound treated.
- the plastic melt is usually caused by a screw in the injection molding cylinder mixed. This mixing of the plastic melt requires a relatively high level mechanical drive power and causes wear and tear on both the Snail as well as on the cylinder.
- the invention has set itself the goal of creating an injection molding machine in which with a structurally simple injection molding unit, the injection resistance of the Melt is reduced. Furthermore, without mechanical means Homogenization of various melt components can also be achieved.
- forces are exerted on the melt which cause it to flow stimulates by using a frequency in the subsonic range a periodic Relative movement between the melting casting cylinder and the material handling unit of the Injection molding machine is generated.
- vibrating elements are provided which either on the injection molding cylinder or on the material feed unit are attached.
- the vibrating elements are connected to a frequency transmitter connected, the frequency transmitter being adjustable in a frequency range, in which the component of the injection molding machine connected to the vibrating element in one preferably harmonic resonance vibration is offset.
- the vibrations are generated in the piezo oscillator (e.g. quartz or barium titanate etc.). These are vibrations that occur along the Spread the injection molding cylinder or the material feed unit.
- the ratio length the material handling unit, e.g. the screw length, to the wavelength of the ultrasound is to be tuned to resonance, otherwise it will not occur at the screw tip Development of the necessary vibration amplitude.
- the piezo element must be kept under tension.
- An advantageous one Design here are proposed clamping screws that hold flanges in to which the piezo encoder is clamped.
- the vibrating element can be connected to the injection molding cylinder.
- the injection molding cylinder including its injection nozzle is off the tool to decouple vibrationally.
- a sliding seal or a is used as a decoupling Damping element proposed.
- the oscillating element is between the Material conveyor unit and the drive arranged. So far the Material conveyor unit is designed as a screw, sliding contacts are to be provided, because the snail also rotates in addition to the transverse movement.
- the Material delivery unit can also be designed as a smooth-walled piston, the is connected to the drive via a drive rod.
- the piston be tubular and the vibrating element in that of the spray nozzle inclined part can be arranged.
- Smooth-walled pistons can be used because the The subject of the invention enables the degree of homogenization of the Ultrasound to forego the mixing function of a snail. This allows with the same homogenization effect as for screw plasticization build a much simpler piston injection unit.
- the third property of ultrasound used in the invention is that Heating up the granules.
- the heat is released mainly at the homogeneity limit points, i.e. where there is still a need for melting.
- the figures each show a movable tool part 11, which has a fixed Tool part 12 forms a mold cavity 13.
- the fixed tool part 12 is with an injection nozzle 25 of an injection molding cylinder 21 connected.
- a material conveying unit 22 is provided in the injection molding cylinder 21 is connected to a drive 51 via a drive rod 52.
- a thermal sensor 81 is provided on the injection molding cylinder is connected to a frequency transmitter 41 via a measuring line 82.
- the material conveying unit 22 is designed as a screw 23 in which A housing 71 is provided at the foot end, which surrounds an oscillating element 31.
- the vibrating element 31 is with the drive rod connected to the drive 51 52 connected.
- Sliding contacts 43 are provided on the drive rod 52 are connected to the frequency transmitter 41 via a connection 42.
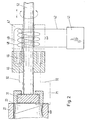
- FIG. 2 shows an inductive coupling of the connection between the generator 41 and the vibrating element 31.
- the frequency generator 41 is over Connections 42 connected to a coil 48, which is in a shell core 47 is arranged.
- the shell core 47 encompasses the one connected to the drive 51 Drive rod 52 and is fixedly connected to the housing of the screw.
- the sink 48 is magnetically connected via a coupling field 49 to a coil 46, which in a shell core 45 is arranged, which is fixed to the drive rod 52.
- the Coil 46 is connected to the oscillating element 31 via connections 32.
- the oscillating element 31 is encompassed by a housing 71, which on the in the Injection molding cylinder 21 provided screw is attached.
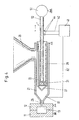
- a vibrating element 31 is provided which is directly connected to the Injection molding cylinder 21 is connected.
- the material conveying unit 22 is designed as a piston 24, the end of which the drive rod 52 connected to the drive 51 is arranged.
- the material conveying unit 22 is designed as a tubular piston 28.
- a Cover 27 At the tip of the tubular piston 28 inclined towards the spray nozzle 25 is a Cover 27 provided.
- the oscillating element 31 is in the area of the cover 27 arranged, which is connected to the drive rod 52.
- the drive rod 52 connected to the drive 51 projects deep into the tubular piston 28.
- Contacts 44 are provided on the drive rod 52, which are connected via the connection 42 are connected to the frequency generator 41.
- the rotation of the present drive rod 52 is limited to a small angle, so that the contacts 44 can be firmly connected and no sliding contacts (cf. Figure 1) are required.
- the RF energy on the ultrasound head according to the principle of inductive transmission be performed.
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Mechanical Engineering (AREA)
- Injection Moulding Of Plastics Or The Like (AREA)
Description
Eine negative Folge der hohen Reibkräfte in der Spritzmasse, die während des Einspritzvorganges zum Ansteigen der Schmelzetemperatur führen, sind teilweise Verbrennungserscheinungen.
- Die Spritzleistung kann durch Verminderung der innermolekularen Reibung in der Schmelze reduziert werden
- Es kann auf teuere und komplizierte Plastifizierschnecken verzichtet werden.
- Die Schmelzehomogenität wird bei Problemmaterial verbessert.
- Bei Einsatz von Kolbenspritzeinheiten kann die Spritzeinheit verkürzt werden.
- Die Mischbarkeit von Zusatzstoffen wie Einfärbmittel und Fremdkomponenten wird verbessert.
- Der Verschleiß an den beweglichen Teilen wird reduziert.
- Die Homogenisierung der Schmelze, insbesondere für optische Anwendungen, wird verbessert.
- Figur 1
- Eine Spritzgießmaschine mit Schnecke und Schwingelement zwischen Schnecke und Antriebsstange.
- Figur 2
- Induktive Kopplung.
- Figur 3
- Eine Spritzgießmaschine mit Kolben mit einem Schwingelement am Spritzgießzylinder.
- Figur 4
- Eine Spritzgießmaschine mit Hohlkolben und dem Schwingelement zwischen Kolben und Antriebsstange.
- 11
- Bewegliches Werkzeugteil
- 12
- Festes Werkzeugteil
- 13
- Formhohlraum
- 21
- Spritzgießzylinder
- 22
- Materialfördereinheit
- 23
- Schnecke
- 24
- Kolben (voll)
- 25
- Spritzdüse
- 26
- Materialzufuhr
- 27
- Deckel
- 28
- Rohrförmiger Kolben
- 31
- Schwingelement
- 32
- Verbindung
- 41
- Frequenzgeber
- 42
- Verbindung
- 43
- Schleifkontakt
- 44
- Kontakt
- 45
- Schalenkern (Welle)
- 46
- Spule (45)
- 47
- Schalenkern (Schneckengehäuse)
- 48
- Spule (47)
- 49
- Koppelfeld
- 51
- Antrieb
- 52
- Antriebsstange
- 61
- Gleitdichtung
- 62
- Dämpfungselement
- 71
- Gehäuse
- 72,73
- Flansche
- 74
- Schraubentemperatur
- 81
- Thermofühler
Claims (13)
- Spritzgießmaschine mit einem Spritzgießzylinder, der fußendig eine trichterförmige Materialzufuhr (26) aufweist und kopfendig mit einer mit einem Werkzeug korrespondierenden Spritzdüse (25) versehen ist,
und einer Materialfördereinheit (22), die an einen Antrieb (51) angeschlossen ist und im Innenraum des Spritzgießzylinders (21) mindestens verschiebbar ist, wobei ein Schwingetement (31) vorgesehen ist, welches eine Retativbewegung zwischen dem Spritzgießzylinder (21) und der Materialfördereinheit (22) erzeugt, das Schwingelement (31) an einen Frequenzgeber (41) angeschlossen ist,
der Frequenzgeber (41) in einem Frequenzbereich einstellbar ist, in dem das mit dem Schwingelement (31) verbundene Bauteil (21, 22) der Spritzgießmaschine in Resonanzschwingung versetzbar ist,
dadurch gekennzeichnet, dass das Schwingelement (31) zwischen der Materialfördereinheit (22) und dem Antrieb (51) angeordnet ist. - Spritzgießmaschine mit einem Spritzgießzylinder, der fußendig eine trichterförmige Materialzufuhr (26) aufweist und kopfendig mit einer mit einem Werkzeug korrespondierenden Spritzdüse (25) versehen ist,
und einer Materialfördereinheit (22), die an einen Antrieb (51) angeschlossen ist und im Innenraum des Spritzgießzylinders (21) mindestens verschiebbar ist, wobei ein Schwingelement (31) vorgesehen ist, welches eine Relativbewegung zwischen dem Spritzgießzylinder (21) und der Materialfördereinheit (22) erzeugt, das Schwingelement (31) an einen Frequenzgeber (41) angeschlossen ist,
der Frequenzgeber (41) in einem Frequenzbereich einstellbar ist, in dem das mit dem Schwingelement (31) verbundene Bauteil (21, 22) der Spritzgießmaschine in Resonanzschwingung versetzbar ist,
dadurch gekennzeichnet, dass das Schwingelement (31) mit dem Spritzgießzylinder (21) verbunden ist,
und der Spritzgießzylinder (21) einschließlich der Spritzdüse (25) vom Werkzeug (12) schwingungsmäßig entkoppelt sind. - Spritzgießmaschine nach Anspruch 2,
dadurch gekennzeichnet, dass die Entkopplung des Spritzgießzylinders (21) einschließlich der Spritzdüse (25) zum Werkzeug (12) als Gleitdichtung (61) ausgestaltet ist. - Spritzgießmaschine nach Anspruch 2,
dadurch gekennzeichnet, dass zwischen der Spritzdüse (25) und dem Spritzgießzylinder (21) ein Dämpfungselement (62) angeordnet ist. - Spritzgießmaschine nach den Ansprüchen 1 oder 2,
dadurch gekennzeichnet, dass das Schwingelement (31) in einem seiner achsialen Längung begrenzenden ein- oder mehrteiligen Gehäuse (71) plaziert ist. - Spritzgießmaschine nach den Ansprüchen 1 oder 2,
dadurch gekennzeichnet, dass das Schwingelement (31) zwischen zwei Flanschen (72, 73) angeordnet ist, und
dass die Flansche (72, 73) über Spannschrauben (74) miteinander unter Vorspannung verbindbar sind. - Spritzgießmaschine nach den Ansprüchen 5 oder 6,
dadurch gekennzeichnet, dass das Schwingetement (31) ein Piezoschwinger ist. - Spritzgießmaschine nach Anspruch 1,
dadurch gekennzeichnet, dass die Materialförciereinheit (22) als Schnecke (23) ausgestaltet ist und
dass in der Verbindung (42) zwischen dem Schwingelement (31) und dem Frequenzgeber (41) ein Schleifkontakt (43) vorgesehen ist. - Spritzgießmaschine nach Anspruch 1,
dadurch gekennzeichnet, dass die Materialfördereinheit (22) als Schnecke (23) ausgestaltet ist und
dass der Frequenzgeber (41) mit einer Spule (48) verbunden ist, die in einem die Antriebsstange (52) umgreifenden Schalenkem (47) angeordnet ist, und
dass die Spule (48) mit einer in einem Schalenkern (45) angeordneten Spule (46) magnetisch gekoppelt ist, die mit dem Schwingelement (31) verbunden ist. - Spritzgießmaschine nach Anspruch 1,
dadurch gekennzeichnet, dass die Materialfördereinheit (22) als Kolben (24) ausgestaltet ist, der über eine Antriebsstange (52) mit dem Antrieb (51) verbunden ist. - Spritzgießmaschine nach Anspruch 1,
dadurch gekennzeichnet, dass die Materialfürdereinheit (22) im wesentlichen als rohrförmiger Kolben (28) ausgestaltet ist und in dem der Spritzdüse (25) zugeneigten Teil durch einen Deckel (27) verschlossen ist, und
dass das Schwingelement (31) zwischen dem Deckel (27) und der Antriebsstange (52) angeordnet ist. - Spritzgießmaschine nach einem der vorgenannten Ansprüche,
dadurch gekennzeichnet, dass mindestens ein Thermoelement (81), welches mit dem Frequenzgeber (41) verbunden ist, zur Erfassung der Temperatur der Schmelze vorgesehen ist. - Spritzgießmaschine nach Anspruch 12,
dadurch gekennzeichnet, dass der Frequenzgeber (41) ein Ultraschallgeber ist, der in einem Frequenzbereich von 10-40 kHz arbeitet.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19802874A DE19802874A1 (de) | 1998-01-20 | 1998-01-20 | Spritzgießmaschine und Verfahren zum Betreiben einer solchen |
| DE19802874 | 1998-01-20 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0930144A2 EP0930144A2 (de) | 1999-07-21 |
| EP0930144A3 EP0930144A3 (de) | 2000-08-23 |
| EP0930144B1 true EP0930144B1 (de) | 2004-06-30 |
Family
ID=7855694
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99250004A Expired - Lifetime EP0930144B1 (de) | 1998-01-20 | 1999-01-05 | Spritzgiessmaschine |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US6203747B1 (de) |
| EP (1) | EP0930144B1 (de) |
| JP (1) | JP3686768B2 (de) |
| AT (1) | ATE270179T1 (de) |
| DE (2) | DE19802874A1 (de) |
Families Citing this family (26)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP3377963B2 (ja) * | 1999-05-28 | 2003-02-17 | 日精樹脂工業株式会社 | 射出成形機用振動付与装置 |
| DE10057741A1 (de) * | 2000-11-16 | 2002-05-23 | Mannesmann Plastics Machinery | Spritzeinheit für eine Kunststoffspritzgießmaschine |
| AU2002245702A1 (en) | 2001-03-19 | 2002-10-03 | Cambridge Polymer Group Inc. | System and methods for reducing interfacial porosity in cements |
| GB0221263D0 (en) * | 2002-09-13 | 2002-10-23 | Dki Plast A S | Apparatus and method for improving the flow characteristics of a material to be injection moulded or extruded |
| JP4446962B2 (ja) * | 2003-07-16 | 2010-04-07 | 出光興産株式会社 | 樹脂材料への超音波振動付与装置、この超音波振動付与装置を用いた樹脂材料の溶融成形方法及び樹脂組成物 |
| US20050236727A1 (en) * | 2004-04-23 | 2005-10-27 | Niewels Joachim J | Method and apparatus for mold component locking using active material elements |
| US20050238757A1 (en) * | 2004-04-23 | 2005-10-27 | Niewels Joachim J | Method and apparatus for assisting ejection from an injection molding machine using active material elements |
| US7481642B2 (en) * | 2004-04-23 | 2009-01-27 | Husky Injection Molding Systems Ltd. | Method and apparatus for controlling a vent gap with active material elements |
| US7165958B2 (en) * | 2004-04-23 | 2007-01-23 | Husky Injection Molding Systems Ltd. | Apparatus for adjustable hot runner assembly seals and tip height using active material elements |
| US20050236725A1 (en) * | 2004-04-23 | 2005-10-27 | Niewels Joachim J | Method and apparatus for countering mold deflection and misalignment using active material elements |
| US7293981B2 (en) * | 2004-04-23 | 2007-11-13 | Husky Injection Molding Systems Ltd. | Apparatus for injection molding using active material elements |
| US7072735B2 (en) * | 2004-04-23 | 2006-07-04 | Husky Injection Molding Systems Ltd. | Control system for utilizing active material elements in a molding system |
| US20050236729A1 (en) * | 2004-04-23 | 2005-10-27 | Arnott Robin A | Method and apparatus for vibrating melt in an injection molding machine using active material elements |
| JP4932600B2 (ja) * | 2007-05-23 | 2012-05-16 | 株式会社フジクラ | 射出成形装置のクリーニング方法 |
| ES2323624B1 (es) | 2007-08-09 | 2011-01-31 | Fundacio Privada Ascamm | Dispositivo ultrasonico para moldeo de micropiezas de plastico. |
| US8313051B2 (en) * | 2008-03-05 | 2012-11-20 | Sealed Air Corporation (Us) | Process and apparatus for mixing a polymer composition and composite polymers resulting therefrom |
| DE102008037103B4 (de) * | 2008-08-08 | 2012-03-01 | Sumitomo (Shi) Demag Plastics Machinery Gmbh | Plastifizierungs- und Einspritzvorrichtung für eine Spritzgießmaschine |
| EP2471644A1 (de) | 2010-12-31 | 2012-07-04 | Fundació Privada Ascamm | System und Verfahren zum Formen von Mikro- und Minikunststoffteilen |
| ES1075859Y (es) | 2011-11-14 | 2012-03-14 | Fundacio Privada Ascamm | Aparato para moldeo de micropiezas de plastico por ultrasonidos |
| DE102013224680A1 (de) * | 2013-12-02 | 2015-06-03 | MAHLE Behr GmbH & Co. KG | Kunststoffspritzgießvorrichtung |
| CN105904699A (zh) * | 2016-04-25 | 2016-08-31 | 顺德职业技术学院 | 带振动芯轴的外螺槽式螺杆挤出装置 |
| GB201819346D0 (en) | 2018-11-28 | 2019-01-09 | Matrix Moulding Systems Ltd | Improvements in ultrasonic injection moulding |
| GB202008355D0 (en) | 2020-06-03 | 2020-07-15 | Matrix Moulding Systems Ltd | Improvements in ultrasonic injection moulding |
| CN112388924B (zh) * | 2020-11-19 | 2025-05-27 | 苏州锦珂塑胶科技有限公司 | 一种转轴式轴向激振装置及注塑机 |
| US20240367362A1 (en) * | 2023-05-02 | 2024-11-07 | Edison Welding Institute, Inc. | Ultrasonically assisted polymer extrusion |
| CN117021511B (zh) * | 2023-09-08 | 2024-11-01 | 玫瑰塑胶(昆山)有限公司 | 一种注塑机用输送管道内材料抗凝装置 |
Family Cites Families (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1186608B (de) * | 1960-10-06 | 1965-02-04 | Ankerwerk Gebr Goller | Schnecken-Spritzgiessmaschine zur Verarbeitung thermoplastischer Kunststoffe |
| JPS5642637A (en) * | 1979-09-14 | 1981-04-20 | Matsushita Electric Works Ltd | Plasticizing and injecting device for injection molder |
| DD152307A1 (de) * | 1980-08-07 | 1981-11-25 | Gerhard Richter | Verfahren und vorrichtung zur homogenisierung von polymerschmelzen |
| CA1243462A (en) * | 1984-12-21 | 1988-10-25 | Peter S. Allan | Moulding process |
| DE3810954A1 (de) * | 1988-03-31 | 1989-10-19 | Kloeckner Ferromatik Desma | Verfahren und vorrichtung zum spritzgiessen von spritzgussteilen aus plastifizierbarem material, insbesondere aus plastifizierbaren fluessigkristall-polymeren |
| JP2673173B2 (ja) * | 1988-05-14 | 1997-11-05 | 株式会社ソディック | 樹脂成形装置 |
| JPH0226722A (ja) * | 1988-07-18 | 1990-01-29 | Toyo Mach & Metal Co Ltd | 射出成形機の射出装置 |
| US5017311A (en) * | 1988-07-21 | 1991-05-21 | Idemitsu Kosan Co., Ltd. | Method for injection molding into a resonating mold |
| US5202066A (en) * | 1989-04-25 | 1993-04-13 | Idemitsu Kosan Co., Ltd. | Method of plasticizing molding material and apparatus therefor |
| CH688822A5 (it) * | 1993-10-11 | 1998-04-15 | Ixtlan Ag | Dispositivo per effettuare il trasferimento allo stato plastico di sostanze con elevato coefficiente di attrito facilitandolo mediante vibrazioni. |
| JP3493878B2 (ja) * | 1996-03-21 | 2004-02-03 | 松下電工株式会社 | 射出成形方法 |
| CN1059626C (zh) * | 1996-07-05 | 2000-12-20 | 华南理工大学 | 电磁式聚合物动态注射成型方法及装置 |
| US5885495A (en) * | 1996-12-19 | 1999-03-23 | Ibar; Jean-Pierre | Viscosity control for molten plastics prior to molding |
-
1998
- 1998-01-20 DE DE19802874A patent/DE19802874A1/de not_active Ceased
-
1999
- 1999-01-05 DE DE59909827T patent/DE59909827D1/de not_active Expired - Lifetime
- 1999-01-05 AT AT99250004T patent/ATE270179T1/de not_active IP Right Cessation
- 1999-01-05 EP EP99250004A patent/EP0930144B1/de not_active Expired - Lifetime
- 1999-01-20 JP JP01124799A patent/JP3686768B2/ja not_active Expired - Fee Related
- 1999-01-20 US US09/234,352 patent/US6203747B1/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| US6203747B1 (en) | 2001-03-20 |
| EP0930144A2 (de) | 1999-07-21 |
| DE59909827D1 (de) | 2004-08-05 |
| DE19802874A1 (de) | 1999-07-22 |
| JP3686768B2 (ja) | 2005-08-24 |
| ATE270179T1 (de) | 2004-07-15 |
| EP0930144A3 (de) | 2000-08-23 |
| JPH11254494A (ja) | 1999-09-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE19802874A1 (de) | Spritzgießmaschine und Verfahren zum Betreiben einer solchen | |
| DE4315076C2 (de) | Ventilgesteuerte Mehrkomponenten-Einspritzdüse mit einer sich drehenden, axialen Betätigungseinrichtung | |
| DE3810954C2 (de) | ||
| DE69912728T2 (de) | Spritzgiessmaschine für thermoplastischen Kunststoff | |
| US5538413A (en) | Apparatus for strengthening weld lines in molded parts | |
| EP0504406A1 (de) | Verfahren und vorrichtung zum spritzgiessen mit filtration und mischen der schmelze. | |
| EP1097035B1 (de) | Spritzgiesseinheit für eine spritzgiessmaschine | |
| DE69703270T2 (de) | Elektromagnetisches dynamisches Spritzgiessverfahren für Polymer und die Vorrichtung dafür | |
| DE10060087C5 (de) | Einspritzaggregat für eine Spritzgießmaschine | |
| DE112005001718T5 (de) | Vertikale Mikrospritzgießmaschine | |
| EP1107855B1 (de) | Verfahren und vorrichtung zum spritzgiessen einer kunststoffmasse | |
| WO2001083192A1 (de) | Einrichtung zum entfernen von spritzgiessteilen | |
| DE4233929A1 (de) | Vorrichtung zur Verbindung von Bauteilen durch Vibrationsschweißung | |
| DE102016125931B4 (de) | Durchflusszelle mit Sonotrode für die Beeinflussung von ruhenden und strömenden Kunststoffschmelzen | |
| NL8105611A (nl) | Extruder voor de vervaardiging van kunststofbuizen. | |
| WO2002087459A2 (de) | Handstück zum linearen antreiben eines vorzugsweise dentalen werkzeuges | |
| CA2455840A1 (en) | Injection molding unit with a device for mixing and metering plastic melt as well as additives | |
| DE102008037103A1 (de) | Plastifizierungs- und Einspritzvorrichtung für eine Spritzgießmaschine | |
| EP1226920B1 (de) | Verfahren zur Herstellung einer Sperrhülse für eine Rückstromsperre einer Kunststoff-Spritzgiessmaschine | |
| SU1729776A1 (ru) | Устройство дл пластикации и впрыска литьевой машины | |
| DE19724346C2 (de) | Vorrichtung zum Plastifizieren und Einspritzen von thermoplastischem Kunststoff | |
| US4805803A (en) | Device for preparing and ejecting a chemically reacting mixture | |
| EP0868987B1 (de) | Vorrichtung zum Plastifizieren und Einspritzen von Thermoplasten in ein Spritzgiesswerkzeug | |
| JPS63288725A (ja) | 射出成形機 | |
| JP2742468B2 (ja) | 樹脂等の混練・射出装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT CH DE FR IT LI |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20010129 |
|
| AKX | Designation fees paid |
Free format text: AT CH DE FR IT LI |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: DEMAG ERGOTECH WIEHE GMBH |
|
| 17Q | First examination report despatched |
Effective date: 20020319 |
|
| RTI1 | Title (correction) |
Free format text: INJECTION MOULDING MACHINE |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: DEMAG ERGOTECH GMBH |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT CH DE FR IT LI |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: E. BLUM & CO. PATENTANWAELTE |
|
| REF | Corresponds to: |
Ref document number: 59909827 Country of ref document: DE Date of ref document: 20040805 Kind code of ref document: P |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20050331 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20060113 Year of fee payment: 8 Ref country code: CH Payment date: 20060113 Year of fee payment: 8 Ref country code: AT Payment date: 20060113 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20060131 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070131 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070131 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20070930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070105 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070105 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20160321 Year of fee payment: 18 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59909827 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170801 |