EP0897020B1 - Endabmessungsnahe Mehrschichtkomponenten einer Verbrennungsvorrichtung, gemäss des Vakuum-Plasmaspritzverfahrens und Verfahren zu dessen Herstellung - Google Patents
Endabmessungsnahe Mehrschichtkomponenten einer Verbrennungsvorrichtung, gemäss des Vakuum-Plasmaspritzverfahrens und Verfahren zu dessen Herstellung Download PDFInfo
- Publication number
- EP0897020B1 EP0897020B1 EP98112560A EP98112560A EP0897020B1 EP 0897020 B1 EP0897020 B1 EP 0897020B1 EP 98112560 A EP98112560 A EP 98112560A EP 98112560 A EP98112560 A EP 98112560A EP 0897020 B1 EP0897020 B1 EP 0897020B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- mold
- component
- layer
- top coat
- vacuum plasma
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 29
- 238000002485 combustion reaction Methods 0.000 title claims description 19
- 238000010290 vacuum plasma spraying Methods 0.000 title claims description 14
- 239000007921 spray Substances 0.000 claims description 28
- 229910000601 superalloy Inorganic materials 0.000 claims description 28
- 239000000919 ceramic Substances 0.000 claims description 27
- 230000007704 transition Effects 0.000 claims description 17
- 238000001816 cooling Methods 0.000 claims description 12
- 238000010438 heat treatment Methods 0.000 claims description 12
- 238000005507 spraying Methods 0.000 claims description 6
- 229910010293 ceramic material Inorganic materials 0.000 claims description 4
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N silicon dioxide Inorganic materials O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 claims description 4
- 239000000377 silicon dioxide Substances 0.000 claims description 4
- 239000000126 substance Substances 0.000 claims description 4
- 229910052742 iron Inorganic materials 0.000 claims description 3
- 229910052759 nickel Inorganic materials 0.000 claims description 3
- 239000012783 reinforcing fiber Substances 0.000 claims description 2
- 229910002077 partially stabilized zirconia Inorganic materials 0.000 claims 1
- MCMNRKCIXSYSNV-UHFFFAOYSA-N Zirconium dioxide Chemical compound O=[Zr]=O MCMNRKCIXSYSNV-UHFFFAOYSA-N 0.000 description 24
- 239000012720 thermal barrier coating Substances 0.000 description 16
- 239000007789 gas Substances 0.000 description 14
- 239000000463 material Substances 0.000 description 14
- 230000008569 process Effects 0.000 description 11
- 238000000151 deposition Methods 0.000 description 9
- 239000000843 powder Substances 0.000 description 8
- 238000000576 coating method Methods 0.000 description 6
- 230000008021 deposition Effects 0.000 description 6
- 238000004519 manufacturing process Methods 0.000 description 6
- 229910052751 metal Inorganic materials 0.000 description 5
- 239000002184 metal Substances 0.000 description 5
- 238000003466 welding Methods 0.000 description 4
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 3
- 229910045601 alloy Inorganic materials 0.000 description 3
- 239000000956 alloy Substances 0.000 description 3
- 230000004888 barrier function Effects 0.000 description 3
- 239000002131 composite material Substances 0.000 description 3
- 229910052802 copper Inorganic materials 0.000 description 3
- 239000010949 copper Substances 0.000 description 3
- 230000003647 oxidation Effects 0.000 description 3
- 238000007254 oxidation reaction Methods 0.000 description 3
- 230000001681 protective effect Effects 0.000 description 3
- 238000000926 separation method Methods 0.000 description 3
- 239000010935 stainless steel Substances 0.000 description 3
- 229910001220 stainless steel Inorganic materials 0.000 description 3
- XKRFYHLGVUSROY-UHFFFAOYSA-N Argon Chemical compound [Ar] XKRFYHLGVUSROY-UHFFFAOYSA-N 0.000 description 2
- 239000011248 coating agent Substances 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 239000000835 fiber Substances 0.000 description 2
- 238000010304 firing Methods 0.000 description 2
- 239000000446 fuel Substances 0.000 description 2
- 229910001026 inconel Inorganic materials 0.000 description 2
- 238000007750 plasma spraying Methods 0.000 description 2
- RUDFQVOCFDJEEF-UHFFFAOYSA-N yttrium(III) oxide Inorganic materials [O-2].[O-2].[O-2].[Y+3].[Y+3] RUDFQVOCFDJEEF-UHFFFAOYSA-N 0.000 description 2
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- 229910001069 Ti alloy Inorganic materials 0.000 description 1
- RTAQQCXQSZGOHL-UHFFFAOYSA-N Titanium Chemical compound [Ti] RTAQQCXQSZGOHL-UHFFFAOYSA-N 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 229910052786 argon Inorganic materials 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 229910000171 calcio olivine Inorganic materials 0.000 description 1
- 229910052918 calcium silicate Inorganic materials 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 239000000788 chromium alloy Substances 0.000 description 1
- 230000007797 corrosion Effects 0.000 description 1
- 238000005260 corrosion Methods 0.000 description 1
- 238000005137 deposition process Methods 0.000 description 1
- 239000003085 diluting agent Substances 0.000 description 1
- 238000005553 drilling Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000003792 electrolyte Substances 0.000 description 1
- 230000007717 exclusion Effects 0.000 description 1
- 229910002804 graphite Inorganic materials 0.000 description 1
- 239000010439 graphite Substances 0.000 description 1
- 229910000856 hastalloy Inorganic materials 0.000 description 1
- 230000000977 initiatory effect Effects 0.000 description 1
- 150000002739 metals Chemical class 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 229910000623 nickel–chromium alloy Inorganic materials 0.000 description 1
- 239000011819 refractory material Substances 0.000 description 1
- 239000003870 refractory metal Substances 0.000 description 1
- 230000003014 reinforcing effect Effects 0.000 description 1
- 230000035939 shock Effects 0.000 description 1
- 239000000779 smoke Substances 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 238000009718 spray deposition Methods 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 230000003746 surface roughness Effects 0.000 description 1
- 239000010936 titanium Substances 0.000 description 1
- 229910052719 titanium Inorganic materials 0.000 description 1
- 238000002604 ultrasonography Methods 0.000 description 1
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/18—After-treatment
- C23C4/185—Separation of the coating from the substrate
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10S—TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10S428/00—Stock material or miscellaneous articles
- Y10S428/922—Static electricity metal bleed-off metallic stock
- Y10S428/9335—Product by special process
- Y10S428/937—Sprayed metal
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12472—Microscopic interfacial wave or roughness
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12535—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.] with additional, spatially distinct nonmetal component
- Y10T428/12611—Oxide-containing component
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12535—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.] with additional, spatially distinct nonmetal component
- Y10T428/12611—Oxide-containing component
- Y10T428/12618—Plural oxides
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12736—Al-base component
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12771—Transition metal-base component
- Y10T428/12861—Group VIII or IB metal-base component
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12771—Transition metal-base component
- Y10T428/12861—Group VIII or IB metal-base component
- Y10T428/12931—Co-, Fe-, or Ni-base components, alternative to each other
Definitions
- This invention relates to improved multilayered combustion system components, such as combustor liners or transition ducts of a gas turbine engine, wherein the inner surface comprises a protective thermal barrier coating (TBC), which includes a ceramic top coat and a metallic bond coat, and the outer surface consists of a structural layer bonded to the TBC through the bond coat.
- TBC protective thermal barrier coating
- the improved qualities of the new components over current components include a superior thermal barrier coating, a better high-temperature structural material, a smoother inside surface, no irregularities (welds) within the component, and excellent reproducibility.
- This is accomplished by a vacuum plasma spray (VPS) process which is used to form the ceramic top coat layer on a suitable mold, followed by a metallic bond coat layer and ending with a structural superalloy layer. Thereafter, the mold is removed to form the multilayered component of the present invention.
- VPS vacuum plasma spray
- TBC's consisting of a ceramic top coat and a metallic bond coat (typically an MCrAlY) on the inner surface of preformed combustion system components.
- a metallic bond coat typically an MCrAlY
- Two of the components protected by such coatings are combustor liners and transition ducts, which contain the combustion flame and channel the extremely hot gas (> 1,300°C) to the first stage vanes.
- the transition ducts in particular have a fairly complex geometry and the presently known technology does not allow for satisfactory coating of internal surfaces of components with such complex geometries.
- combustion system components such as combustor liners and transition ducts
- the current fabrication process of combustion system components consists of: (i) mechanically forming two or more individual sections of the component; (ii) plasma spraying by atmospheric plasma spray (APS) the inner surface of each section to form the thermal barrier coating system; (iii) welding the sections so coated; (iv) plasma spraying by APS the protective TBC coatings on the welds whenever possible; and, for transition ducts, (v) laser drilling cooling holes through the structural wall and the coating.
- APS atmospheric plasma spray
- APS plasma spraying by APS the protective TBC coatings on the welds whenever possible
- laser drilling cooling holes through the structural wall and the coating.
- Weld regions act as weak sites from which failure may initiate due to poor quality finish of both the top coat and the bond coat of the TBC. Also, due to the rough surface of the TBC inherent in the APS process and particularly of the weld regions, an undesirable change in flow pattern of the hot gas is often produced. Moreover, because the current fabricating process consists of mechanically forming sections of the component followed by welding and spraying inner surfaces of these sections, there is a limitation on the choice of suitable superalloys. Only superalloys with high elongation such as, nickel-chromium alloys known under trade names Haynes 230, IN-617, etc. are suitable. Superalloys which do not possess the required elongation or ductility cannot be used with the current fabrication process, even if they possess other superior properties, such as better high temperature strength and creep resistance, e.g. IN-738LC superalloy.
- HPTEI High Performance Turbine Engine Initiative
- ATS Advanced Turbine System
- Gas turbine hot-section materials constitute an important limiting factor and are critical to achieving the higher firing temperatures.
- Current methods of producing closed combustion system components, e.g., combustor liners and transition ducts, to contain and guide the hot gas, have inherent limitations which are difficult to overcome, especially in more demanding conditions, such as higher temperatures and pressures.
- Another object is to provide combustion system components which resist high gas temperatures of the order of 800°C - 1600°C.
- a still further object of the present invention is to form components with a protective inner TBC, which do not require welding as an integral part of the fabrication process.
- novel components of the present invention are near net-shape VPS formed multilayered combustion system components, such as combustor liners or transition ducts, which comprise:
- the ceramic top coat is normally of a thickness greater than 250 ⁇ m and preferably greater than 1 mm.
- the preferred range of the top coat thicknesses is between 1 and 1.5 mm.
- It is formed of ceramic materials such as zirconia (ZrO 2 ) and calcia-silica (Ca 2 SiO 4 ).
- ZrO 2 may be partially stabilized with yttria (Y 2 O 3 ) as is known in the art.
- the metallic bond coat is made of MCrAlY where M is Ni, Co, Fe or a combination thereof.
- M is Ni, Co, Fe or a combination thereof.
- CoNiCrAlY is an excellent bond coat material when sprayed to a thickness of between about 100 - 200 ⁇ m.
- Such material is already described, for example, in U.S. patent No. 5,384,200 of January 24, 1995, where it is deposited as part of a TBC on the surface of combustion chamber components by plasma spray; the components themselves in that case are, however, not formed by plasma spray and furthermore no use of VPS is disclosed.
- the near net-shape VPS formed outer structural superalloy layer is normally formed of a nickel-base or cobalt-base superalloy having good structural and thermal resistance properties, such as Inconel, Hastelloy or Haynes Alloy, however, unlike known technology where such alloys had to be mechanically preformed and, therefore, had to possess sufficient elongation and ductility for that purpose; in the present case, any desired superalloy may be employed, since the outer structure is also formed in accordance with the present invention by vacuum plasma spray unlike anything taught by the prior art for such multilayered applications.
- a superalloy such as IN-738LC which has excellent high temperature resistance properties, but is too brittle to be mechanically formed, can now be used within the present invention.
- the structural superalloy layer is usually between 1 and 5 mm thick, and should be capable of withstanding temperatures in excess of 700 °C. Because it is formed by VPS, it has no seams or welds and it may be deposited to different predetermined thicknesses within the same component, which is very useful for components with complex geometries, such as the transition duct, where it may be desirable to have a thicker structure wall in some areas of the component. Such thicker build-ups may be spray formed, according to this invention, within the same overall operation, i.e. when the entire multilayered structure of the component is being formed.
- Both the bond coat and the structural layer are normally built-up with dense microstructures, typically less than 1.5% porosity and preferably less than 1% porosity, whereas the top coat will usually be produced with a controlled porosity of between 5 and 20%, (e.g. 10%) to maximize its thermal barrier properties.
- reinforcing continuous fibers may be incorporated in any of the layers to improve the mechanical properties of the component. This is accomplished by providing a spool within the vacuum plasma spray chamber from which the fibers are fed while deposition of the layers is carried out.
- the present invention also includes a method of near net-shape forming by VPS of the multilayered combustion system components described above which comprises:
- the mold may be a destructible mold, which means that after each operation it will be destroyed by removing it, for example, through chemical or electrochemical means. In such a case it is usually made of a soft metal, such as copper, and is used with components of complex geometries from which it cannot be mechanically withdrawn after cooling.
- the mold may be a re-usable mold, in which case it will be made of steel (eg. stainless steel), graphite or other suitable material which, after cooling is mechanically removed, and which may then be re-used to make further components.
- the mold may be either solid or hollow.
- the mold should have a smooth surface, such as to enable VPS forming of components with smooth inside surface, and it should be capable of withstanding and operating at high temperatures.
- the method of the present invention would comprise the following steps:
- the mold is usually heated to a surface temperature of about 400°C - 700°C prior to spraying the top coat layer thereon, however, if a debonding layer is first sprayed onto the mold, the mold is normally heated to a surface temperature below 400°C when applying the debonding layer, although one may start applying such layer even when the mold has not been preheated, since the surface of the mold will be rapidly heated by the plasma torch used to apply the debonding layer.
- the torch heating may be assisted using heat from another source, such as infrared lamps directed towards the mold, or when the mold is hollow, a heating coil may be placed within such hollow mold to provide additional heat when required.
- thermally insulate regions of the mold which do not require deposition e.g. the two ends of the cylindrical mold used to form combustor liners, may be capped with ceramic prior to the VPS operation.
- the ceramic top coat layer which may consist of a mixture of ZrO 2 and Ca 2 SiO 4 , is usually deposited to a thickness of between 250 ⁇ m and 1.5 mm depending on thermal barrier requirements.
- the porosity of the ceramic top coat is also normally controlled so as to maximize its thermal barrier properties.
- the most commonly employed top coat is ZrO 2 because it has a very low thermal conductivity, however, it cannot be deposited to thicknesses above about 250 ⁇ m because it will then have a tendency to spall. It has been found that admixtures of ZrO 2 with Ca 2 SiO 4 obviate this problem and allow much thicker top coat deposits.
- Ca 2 SiO 4 has about twice the thermal conductivity of ZrO 2 , an admixture thereof with zirconia allows to increase the thickness of the top coat layer, and the higher the quantity of calcia-silica, the thicker the top coat layer that can be built-up.
- the ceramic top coat layer has been produced, its surface is normally heated to about 700°C - 800°C prior to applying the metallic bond coat, which is built-up to a thickness of between about 100 ⁇ m and 200 ⁇ m, typically about 150 ⁇ m. Then, after formation of the bond coat, whose surface temperature is maintained at about 700°C - 800°C, the metallic structural layer of e.g. IN-738LC superalloy is vacuum plasma sprayed to a thickness of between 1 and 5 mm.
- the metallic structural layer of e.g. IN-738LC superalloy is vacuum plasma sprayed to a thickness of between 1 and 5 mm.
- the final step in the present VPS net-shape forming method is the cooling of the obtained structure and the removal of the mold from the produced multilayered component.
- the multilayered component such as the combustor liner
- the mold will detach itself from the mold at the debonding layer during the cool down of the structure. It is at this point that the mold is removed mechanically from the near net-shape component.
- the mold is removed chemically or electrochemically by selecting a good etchant or electrolyte which will quickly disintegrate the mold material, but without affecting the VPS formed layers.
- the resulting near net-shape formed multilayered component has a smooth thermal barrier coating as its inside surface and a good, strong structural layer for example of IN-738LC superalloy as its outer structure.
- the component may also be heat treated to further improve the mechanical properties of the structural layer or may be machined down to a smaller size of outer dimensions. Due to the use of smooth mold surface and of the VPS process, a very high smoothness of the inside surface may be achieved, normally less than 25 ⁇ m R z , which to applicants' knowledge is not achievable by any other process and is unknown in this type of components.
- this debonding layer should be sufficiently strong to provide enough adhesion between the mold and the top coat to allow for the build-up of the entire multilayered component, whereas the second role is that this debonding layer should be weak enough for allowing detachment or debonding of the mold from the final component upon subsequent cooling of the structure.
- the debonding layer is normally made of the same material as the top coat (or some similar compatible material that will satisfy the above requirements) and is vacuum plasma sprayed at a relatively low temperature (usually below 400 °C) with spray parameters that form a cooler and faster plasma jet. These spray conditions provide enough adhesion at the mold surface for the required build-up, but not high enough to maintain the bond during cool down.
- the difference in the coefficient of thermal expansion between the mold (high CTE) and the ceramic top coat (lower CTE) creates a tensile stress greater than the adhesive or cohesive bond strength at the debonding layer region leading to separation of the two.
- the debonding layer Once the debonding layer has been applied to the mold, the latter is heated to a temperature of between about 400°C and 700°C prior to applying the top coat.
- This also plays two roles, one being an improved adhesion of the further deposits and the controlling of stress within the coatings at their interfaces, and the other being the expansion of the mold prior to build-up of the various layers, which facilitates removal of the mold when it contracts during the subsequent cool down.
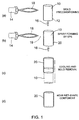
- step (a) mold 10 is preconditioned by applying a thin debonding layer 12 thereto through vacuum plasma spraying of this debonding layer with the plasma torch 14. This is done at a relatively low temperature of less than 400°C with 2-4 passes of the plasma jet 18 effected by rotation of the mold 10 using rotating means 16. Thereafter, the mold 10 is heated using jet 18 of the same plasma torch 14, to a temperature of between 400°C and 700°C.
- step (b) the various layers of the multilayered component 20, starting with the inner TBC and ending with the outer structural layer are spray formed by VPS through successive deposits of such layers using plasma torch 14 emitting plasma jet 18 and various powders 19, while rotating the structure by rotating means 16 to successively deposit the multilayered component 20.
- the temperature and vacuum conditions as well as other spray parameters are adjusted as needed between deposition of the successive layers.
- step (c) the structure is cooled down and mold 10 is mechanically removed from the multilayered component 20 from which it can be readily separated due to the existence Of debonding layer 12 deposited in step (a).
- the near net-shape component 20 is obtained in step (d) where it can optionally be heat treated to improve the mechanical properties of the outer structural layer made, for instance, of Inconel or IN-738LC superalloy, and/or it can be machined down to a smaller size.
- the mold has a complex geometry such as that of the transition duct, the mold can then be made of a soft metal, such as copper, and no deposition of the debonding layer is required in step (a) where the mold is simply heated to the desired temperature of between 400°C - 700°C. In step (c) such mold is removed by disintegration via chemical or electrochemical means as already mentioned previously.
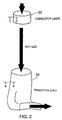
- Fig. 2 illustrates an arrangement of a combustor liner 22 and a transition duct 24 and shows by a thick arrow the passage of the hot gas therethrough.
- a turbine between the combustor liner 22 and the transition duct 24, there are normally provided additional combustor liners forming the so called combustor basket.
- the compressor discharge air is mixed with the fuel combusted near the top of the combustor basket.
- the basket is designed to contain the flame, to mix-in diluent air, to control temperature emissions and smoke, to channel the hot gases into the turbine, and to provide for air cooling of the metal walls.
- the combustor liner 22 and the transition duct 24 have been near net-shape formed by VPS in accordance with the present invention and have a multilayered structure shown in cross-section in Fig. 3 for the combustor liner made with a re-usable mold and in Fig. 4 for the transition duct made with a destructible mold.
- the cross-section shows a thin remainder 26 of the debonding layer left after removal of the mold. It is usually made of a ceramic material, such as ZrO 2 , and is ⁇ 0.01 mm in thickness. It effectively becomes part of the ceramic top coat 28, since it is generally made of the same material as the top coat, except that it is sprayed onto the mold at a lower surface temperature than the top coat, namely with the surface temperature of the mold being about 300°C - 400°C, although the spraying may begin without preheating the mold. Then, top coat 28 is sprayed onto the debonding layer 26 after heating said debonding layer to a temperature between 400°C and 700°C.
- the top coat 28 may, for example, be made of ZrO 2 -Ca 2 SiO 4 admixture and normally has a thickness > 1mm.
- a metallic bond coat 30 is sprayed thereon after heating the surface 29 of the top coat 28 to a temperature of between about 700°C and 800°C.
- This bond coat 30 may, for example, be made of CoNiCrAlY alloy and has a thickness of ⁇ 0.15 mm.
- this bond coat 30 has been deposited, its surface 31 is preheated to or maintained at a temperature between about 700°C and 800°C and a structural layer 32 is then sprayed thereon.
- This structural layer 32 may be made, for instance, of superalloy IN-738LC and has a thickness of, for example, 1 - 5 mm.
- Fig. 4 illustrates a structure similar to that of Fig. 3, but made using a destructible mold, for instance made of copper, which is later removed by destroying it through chemical or electrochemical means.
- a destructible mold for instance made of copper, which is later removed by destroying it through chemical or electrochemical means.
- no initial debonding layer is applied, but rather the top coat 28 is directly applied to a mold preheated between 400°C and 700°C .
- bond coat 30 and structure layer 32 are successively applied as already described with reference to Fig. 3. It should be mentioned that additional desired layers or coatings, including reinforcing fibers, may be incorporated into the structure.
- This example illustrates the fabrication of a combustor liner according to the present invention.
- a mold of stainless steel 304 was used for this example.
- the outer diameter of the mold was machined so as to achieve a near net-shape of the inner diameter of the desired combustor liner, taking into account the mold expansion factor (determined from previous trials). In this case, it was machined so as to achieve a combustor liner of 18 cm internal diameter.
- the mold surface was grit blasted and ultrasound cleaned prior to its introduction into the VPS chamber. Upon closing the chamber door, the system was pumped down to 6 x 10 -3 mbar.
- the spray formed part was physically removed from the mold.
- the part had an overall wall thickness of approximately 6.4 mm, and an inside surface roughness of approximately 19.1 ⁇ m R z .
- the structural superalloy layer was then machined down to achieve an overall wall thickness of 4.5 mm.
- cylindrical combustor liners are used in can-type combustors.
- Several combustor liners are arranged around the engine, with the can axis more or less parallel to the shaft.
- Primary combustion air and fuel are injected at one end of the can and combust. some of the primary combustion air flows over the outside of the liner and enters through nozzles downstream. Secondary and tertiary air, passes over the outside of the primary combustor liner, thus providing some cooling.
- Combustor liners undergo abrupt temperature fluctuations resulting in low cycle fatigue (LCF); the combustion process generates high-frequency vibrations which can also induce high cycle fatigue (HCF) failures.
- the relatively thin walls of the conventional liners make oxidation of the structural alloy a concern.
- the pressure outside the combustor liner is higher than the inside, which enables the secondary and tertiary air flow through the wall perforations. This difference in pressure, in combination with the thin-nature of the liner wall, may lead to creep problems for the component.
- the weld in the liner wall and the roughness of its internal surface also represent problems that have already been discussed above.
- a combustor liner with a thicker, more uniform, and smoother TBC can be fabricated to better resist the low cycle fatigue, high cycle fatigue, oxidation, and creep.
- Other improvements include: better superalloy material for structural layer; exclusion of welding from the fabrication process; and lower temperature exposure of superalloy.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Plasma & Fusion (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Coating By Spraying Or Casting (AREA)
Claims (11)
- Endabmessungnahe Komponente von Verbrennungseinrichtungen, die durch Vakuumplasmaspritzen geformt ist, beispielsweise eine Brennkammerauskleidung (22) oder eine Übergangs- bzw. Transitionsführung (24) einer Gasturbine, umfassend:a. einen inneren keramischen Decküberzug (28) mit einer gleichförmigen Dicke zwischen 0,25 mm und 1,5 mm sowie einer glatten Innenfläche;b. einen zwischengeschalteten metallischen Haftüberzug (30) aus MCrAIY, wo M gleich Ni, Co, Fe oder eine Kombination hiervon mit einer Dicke zwischen 0,1 mm und 0,2 mm, die geringer als die des keramischen Decküberzugs (28) ist, bedeutet; undc. eine äußere Superlegierungsstrukturschicht (32) mit einer Dicke zwischen 1 mm und 5 mm, die innerhalb der Komponente variieren kann und in der Lage ist, Temperaturen oberhalb 700°C auszuhalten, wobei diese äußere Strukturschicht (32) keinerlei Nähte oder Schweißungen irgend einer Art darin hat.
- Komponente nach Anspruch 1, wobei der keramische Decküberzug (28) gewählt ist aus teilweise stabilisiertem Zirkoniumoxid, Kalziumoxld-Siliziumoxid und einer Kombination hiervon, aufgetragen mit einer Porosität von 5 - 20 %.
- Komponente nach Anspruch 1 oder 2, wobei die glatte Innenfläche des keramischen Decküberzugs (28) über eine Rauheit von weniger als 25 µm Rz verfügt.
- Komponente nach Anspruch 1, 2 oder 3, wobei die Superlegierungsstruktur (32) eine Superlegierung auf Nickelbasis oder Kobaltbasis mit guten Eigenschaften hinsichtlich Struktur und thermischer Beständigkeit ist.
- Verfahren zum Formen einer endabmessungnahen Komponente eines Mehrschichtverbrennungssystems durch Vakuumplasmaspritzen, wobei die Komponente über wenigstens einen inneren keramischen Decküberzug (28), einen zwischengeschalteten metallischen Haftüberzug (30) und eine äußere Superlegierungsstrukturschicht (32) verfügt, umfassend:a. Vorsehen einer Form (10) innerhalb einer Vakuumplasmaspritzkammer, wobei die Form über die Gestalt der Innenfläche der gewünschten Komponente verfügt;b. Erwärmen dieser Form (10) auf einer Oberflächentemperatur von 400°C - 700°C und Vakuumplasmaspritzen dieser Form mit dem keramischen Decküberzug (28), bis eine gewünschte Dicke hiervon erreicht ist;c. dann Erwärmen des so erzeugten keramischen Decküberzugs (28) auf eine Oberflächentemperatur zwischen 700°C und 800°C oder Aufrechterhalten einer solchen Temperatur und Vakuumplasmaspritzen hierauf einer dünnen Schicht des metallischen Haftüberzugs (30);d. anschließendes Vakuumplasmaspritzen auf dem so erzeugten Haftüberzug (30), der auf einer Temperatur zwischen 700°C und 800°C gehalten ist, der Superlegierungsstrukturschicht (32), bis eine gewünschte Dicke hiervon erreicht ist; unde. Kühlen der so erzeugten Struktur und Entfernen der Form (10) hiervon, derart, dass die endabmessungsnahe Mehrschichtkomponente von innen nach außen in einem einzigen Gesamtvorgang geformt wird.
- Verfahren nach Anspruch 5, wobei die Form (10) wieder verwendbar ist und wobei eine dünne Trennschicht (26) aus keramischem Material im Vakuumplasma-Spritzverfahren hierauf vor dem Spritzen der keramischen Deckschicht (28) aufgebracht wird.
- Verfahren nach Anspruch 5, die Verwendung einer zerstörbaren Form für Komponenten (24) von komplexer geometrischer Gestalt umfassend, wobei die Form nach dem Kühlen der Struktur durch chemische oder elektrochemische Mittel entfernt wird.
- Verfahren nach Anspruch 5, wobei das Erwärmen der Form unter Zuhilfenahme einer äußeren Wärmequelle durchgeführt wird.
- Verfahren nach Anspruch 8, wobei die Form (10) hohl ist und die äußere Heizquelle eine in die hohle Form eingeführte Heizspule ist.
- Verfahren nach einem der Ansprüche 5 bis 9, wobei Verstärkungsfasern in wenigstens eine Schicht der Komponente (22, 24) zur Verbesserung von deren mechanischen Eigenschaften eingearbeitet werden.
- Verfahren nach einem der Ansprüche 5 bis 10, wobei die erzeugte Komponente zur Verbesserung der mechanischen Eigenschaften der Strukturschicht (32) wärmebehandelt wird.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CA2211961 | 1997-07-29 | ||
| CA002211961A CA2211961C (en) | 1997-07-29 | 1997-07-29 | Near net-shape vps formed multilayered combustion system components and method of forming the same |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0897020A1 EP0897020A1 (de) | 1999-02-17 |
| EP0897020B1 true EP0897020B1 (de) | 2003-10-08 |
Family
ID=4161153
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98112560A Expired - Lifetime EP0897020B1 (de) | 1997-07-29 | 1998-07-07 | Endabmessungsnahe Mehrschichtkomponenten einer Verbrennungsvorrichtung, gemäss des Vakuum-Plasmaspritzverfahrens und Verfahren zu dessen Herstellung |
Country Status (4)
| Country | Link |
|---|---|
| US (2) | US6087023A (de) |
| EP (1) | EP0897020B1 (de) |
| CA (1) | CA2211961C (de) |
| DE (1) | DE69818769T2 (de) |
Families Citing this family (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CA2211961C (en) * | 1997-07-29 | 2001-02-27 | Pyrogenesis Inc. | Near net-shape vps formed multilayered combustion system components and method of forming the same |
| CA2229124C (en) * | 1998-02-09 | 2001-08-14 | Pyrogenesis Inc. | Thermal barrier coating system having a top coat with a graded interface |
| DE10131362A1 (de) | 2001-06-28 | 2003-01-09 | Alstom Switzerland Ltd | Verfahren zur Herstellung einer räumlich geformten, folienartig ausgebildeten Trägerschicht aus sprödhartem Material |
| FR2854166B1 (fr) * | 2003-04-25 | 2007-02-09 | Snecma Moteurs | Procede d'obtention d'une barriere thermique flexo-adaptative |
| US7144602B2 (en) | 2003-04-25 | 2006-12-05 | Snecma Moteurs | Process for obtaining a flexible/adaptive thermal barrier |
| EP1645654A1 (de) * | 2004-05-18 | 2006-04-12 | Snecma | Verfahren zum Herstellen einer flexiblen Wärmedämmschich |
| US7493691B2 (en) * | 2004-05-20 | 2009-02-24 | Honeywell International Inc. | Co-molding metallic-lined phenolic components |
| US7378132B2 (en) * | 2004-12-14 | 2008-05-27 | Honeywell International, Inc. | Method for applying environmental-resistant MCrAlY coatings on gas turbine components |
| US9103035B2 (en) | 2013-04-10 | 2015-08-11 | General Electric Company | Erosion resistant coating systems and processes therefor |
| US9695697B2 (en) * | 2013-09-25 | 2017-07-04 | General Electric Company | Erosion shield, method of fabricating a shield, and method of fabricating an article having a shield |
| JP6421525B2 (ja) * | 2013-10-09 | 2018-11-14 | 信越化学工業株式会社 | 溶射成形体の製造方法 |
| US20150275682A1 (en) * | 2014-04-01 | 2015-10-01 | Siemens Energy, Inc. | Sprayed haynes 230 layer to increase spallation life of thermal barrier coating on a gas turbine engine component |
| JP6741403B2 (ja) * | 2015-07-14 | 2020-08-19 | 株式会社エムダップ | 医療器具の製造装置及び医療器具の製造方法 |
| US10670269B2 (en) * | 2016-10-26 | 2020-06-02 | Raytheon Technologies Corporation | Cast combustor liner panel gating feature for a gas turbine engine combustor |
| US10823410B2 (en) * | 2016-10-26 | 2020-11-03 | Raytheon Technologies Corporation | Cast combustor liner panel radius for gas turbine engine combustor |
Family Cites Families (22)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3204917A (en) * | 1960-12-16 | 1965-09-07 | Owens Illinois Glass Co | Layered mold |
| US3427698A (en) * | 1965-11-26 | 1969-02-18 | Chandler Evans Inc | Rocket nozzle |
| US3467583A (en) * | 1966-05-16 | 1969-09-16 | Camin Lab | Process for making a hollow body with protective inner layer for high-temperature applications |
| DE2809709C3 (de) * | 1978-03-07 | 1982-03-25 | Messerschmitt-Bölkow-Blohm GmbH, 8000 München | Verfahren zur Herstellung eines mindestens eine Keramikschicht aufweisenden Schutzüberzugs für thermisch hochbelastete Bauteile, insbesondere Waffenkomponenten |
| DE2914894C2 (de) | 1979-04-12 | 1980-07-24 | Klein, Schanzlin & Becker Ag, 6710 Frankenthal | Kreiselpumpe |
| FR2498123A1 (fr) * | 1981-01-19 | 1982-07-23 | Matra | Procede de fabrication de pieces metalliques de forme par projection sur un modele destructible |
| FR2559506A1 (fr) * | 1984-02-14 | 1985-08-16 | Reparation Mat Aero Const | Procede de realisation de pieces creuses par projection plasma |
| US4577431A (en) * | 1984-05-02 | 1986-03-25 | General Electric Company | Wear resistant gun barrel and method of forming |
| DE3513882A1 (de) * | 1985-04-17 | 1986-10-23 | Plasmainvent AG, Zug | Schutzschicht |
| JPS61288060A (ja) * | 1985-06-13 | 1986-12-18 | Sumitomo Electric Ind Ltd | 減圧プラズマア−ク溶射方法 |
| US4743462A (en) * | 1986-07-14 | 1988-05-10 | United Technologies Corporation | Method for preventing closure of cooling holes in hollow, air cooled turbine engine components during application of a plasma spray coating |
| US5498484A (en) * | 1990-05-07 | 1996-03-12 | General Electric Company | Thermal barrier coating system with hardenable bond coat |
| CA2038273A1 (en) * | 1990-06-29 | 1991-12-30 | Paul A. Siemers | Tube fabrication with reusable mandrel |
| RU2053310C1 (ru) * | 1991-01-14 | 1996-01-27 | Всероссийский научно-исследовательский институт авиационных материалов | Способ защиты деталей сложной формы из никелевых сплавов |
| DE4114962A1 (de) * | 1991-05-04 | 1992-11-05 | Univ Chemnitz Tech | Verfahren zur herstellung von multilayerschichten |
| AU3323193A (en) * | 1991-12-24 | 1993-07-28 | Detroit Diesel Corporation | Thermal barrier coating and method of depositing the same on combustion chamber component surfaces |
| JPH06101012A (ja) * | 1992-08-03 | 1994-04-12 | Toyota Motor Corp | 内面溶射方法 |
| US5332601A (en) * | 1992-12-10 | 1994-07-26 | The United States As Represented By The United States Department Of Energy | Method of fabricating silicon carbide coatings on graphite surfaces |
| JP2991991B2 (ja) * | 1997-03-24 | 1999-12-20 | トーカロ株式会社 | 耐高温環境用溶射被覆部材およびその製造方法 |
| CA2211961C (en) * | 1997-07-29 | 2001-02-27 | Pyrogenesis Inc. | Near net-shape vps formed multilayered combustion system components and method of forming the same |
| US5817372A (en) * | 1997-09-23 | 1998-10-06 | General Electric Co. | Process for depositing a bond coat for a thermal barrier coating system |
| CA2229124C (en) * | 1998-02-09 | 2001-08-14 | Pyrogenesis Inc. | Thermal barrier coating system having a top coat with a graded interface |
-
1997
- 1997-07-29 CA CA002211961A patent/CA2211961C/en not_active Expired - Lifetime
-
1998
- 1998-07-07 DE DE69818769T patent/DE69818769T2/de not_active Expired - Lifetime
- 1998-07-07 EP EP98112560A patent/EP0897020B1/de not_active Expired - Lifetime
- 1998-07-14 US US09/114,893 patent/US6087023A/en not_active Expired - Lifetime
-
2000
- 2000-04-28 US US09/560,807 patent/US6296723B1/en not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| CA2211961C (en) | 2001-02-27 |
| US6087023A (en) | 2000-07-11 |
| DE69818769T2 (de) | 2004-08-05 |
| EP0897020A1 (de) | 1999-02-17 |
| DE69818769D1 (de) | 2003-11-13 |
| US6296723B1 (en) | 2001-10-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2211961C (en) | Near net-shape vps formed multilayered combustion system components and method of forming the same | |
| US6355356B1 (en) | Coating system for providing environmental protection to a metal substrate, and related processes | |
| US5732467A (en) | Method of repairing directionally solidified and single crystal alloy parts | |
| JP4108152B2 (ja) | 保護皮膜を有する流体冷却製品並びにその製造方法 | |
| EP1428908B1 (de) | Wärmedämmschicht (TBC), welche durch eine thermisch glasierte Schicht geschützt ist, und Verfahren zu ihrer Herstellung | |
| EP0968316B1 (de) | Verfahren zur behandlung von metallteilen | |
| EP0808913B1 (de) | Verfahren zur Reparatur einer Wärmesperrschicht | |
| CN102953828B (zh) | 带有冷却通道的构件和制造方法 | |
| EP1908856B2 (de) | Segmentierte abreibbare Beschichtungen und Verfahren zu ihrer Anwendung | |
| EP0605196A1 (de) | Verfahren zum Aufbringen einer Wärmedämmschicht | |
| EP1054077B1 (de) | Werkstück aus Titan mit Schutzbeschichtung und Verfahren zum Aufbringen einer Schutzschicht auf ein Werkstück aus Titan | |
| US6165628A (en) | Protective coatings for metal-based substrates and related processes | |
| US6180260B1 (en) | Method for modifying the surface of a thermal barrier coating, and related articles | |
| CN101108454A (zh) | 涂覆制品的修复方法 | |
| Movchan | EB-PVD technology in the gas turbine industry: present and future | |
| JPH11229161A (ja) | 遮熱コーティング系用ボンディングコートの緻密化及び粒子間結合の促進方法 | |
| JP2012102731A (ja) | 一時的被覆を使用して構成部品を作製する方法 | |
| EP1881154B1 (de) | Reparaturverfahren für beschichtete Artikel | |
| JP2007231422A (ja) | コーティング方法、およびコーティングされた物品 | |
| GB2474345A (en) | Fabricating and repairing turbine rotors by cold spraying powder | |
| CA1298147C (en) | Thermal spray coating having improved adherence, low residual stress andimproved resistance to spalling and methods for producing same | |
| US20030203224A1 (en) | Thermal barrier coating of intermediate density | |
| EP1390549A1 (de) | Metall-zirconium-verbundbeschichtung | |
| Rickerby et al. | Coatings for gas turbines | |
| WO2008140588A1 (en) | Method for producing an environmentally-resistant thermal barrier coating system on a component |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): CH DE FR GB IT LI SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 19990727 |
|
| AKX | Designation fees paid |
Free format text: CH DE FR GB IT LI SE |
|
| 17Q | First examination report despatched |
Effective date: 20000922 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RTI1 | Title (correction) |
Free format text: NEAR NET-SHAPE MULTILAYERED COMBUSTION SYSTEM COMPONENTS FORMED BY VACUUM PLASMA SPRAYING AND METHOD OF FORMING THE SAME |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE FR GB IT LI SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031008 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20031008 Ref country code: CH Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031008 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 69818769 Country of ref document: DE Date of ref document: 20031113 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040108 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040709 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20130723 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20130719 Year of fee payment: 16 Ref country code: FR Payment date: 20130730 Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69818769 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20140707 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20150331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150203 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69818769 Country of ref document: DE Effective date: 20150203 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140707 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140731 |