EP0631822B1 - Vorrichtung zum maschinellen Auftragen von pastösem Material auf eine zu bearbeitende Fläche - Google Patents
Vorrichtung zum maschinellen Auftragen von pastösem Material auf eine zu bearbeitende Fläche Download PDFInfo
- Publication number
- EP0631822B1 EP0631822B1 EP94104125A EP94104125A EP0631822B1 EP 0631822 B1 EP0631822 B1 EP 0631822B1 EP 94104125 A EP94104125 A EP 94104125A EP 94104125 A EP94104125 A EP 94104125A EP 0631822 B1 EP0631822 B1 EP 0631822B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- application
- compressed air
- opening
- drain line
- application nozzle
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images

Classifications
-
- E—FIXED CONSTRUCTIONS
- E04—BUILDING
- E04F—FINISHING WORK ON BUILDINGS, e.g. STAIRS, FLOORS
- E04F21/00—Implements for finishing work on buildings
- E04F21/02—Implements for finishing work on buildings for applying plasticised masses to surfaces, e.g. plastering walls
- E04F21/06—Implements for applying plaster, insulating material, or the like
- E04F21/08—Mechanical implements
- E04F21/12—Mechanical implements acting by gas pressure, e.g. steam pressure
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B7/00—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas
- B05B7/02—Spray pistols; Apparatus for discharge
- B05B7/12—Spray pistols; Apparatus for discharge designed to control volume of flow, e.g. with adjustable passages
- B05B7/1254—Spray pistols; Apparatus for discharge designed to control volume of flow, e.g. with adjustable passages the controlling means being fluid actuated
- B05B7/1263—Spray pistols; Apparatus for discharge designed to control volume of flow, e.g. with adjustable passages the controlling means being fluid actuated pneumatically actuated
- B05B7/1272—Spray pistols; Apparatus for discharge designed to control volume of flow, e.g. with adjustable passages the controlling means being fluid actuated pneumatically actuated actuated by gas involved in spraying, i.e. exiting the nozzle, e.g. as a spraying or jet shaping gas
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B13/00—Machines or plants for applying liquids or other fluent materials to surfaces of objects or other work by spraying, not covered by groups B05B1/00 - B05B11/00
- B05B13/005—Machines or plants for applying liquids or other fluent materials to surfaces of objects or other work by spraying, not covered by groups B05B1/00 - B05B11/00 mounted on vehicles or designed to apply a liquid on a very large surface, e.g. on the road, on the surface of large containers
Definitions
- the invention relates generally to a device for the mechanical application of pasty material, in particular a processing gun for applying adhesive and reinforcing mortar to mineral fiber insulation boards, such as. B. from DE-A-39 16 319 (cf. preamble of claim 1) known.
- Application nozzle devices are known from the processing of (mineral) thermal plaster, to which the pasty thermal plaster is fed via a conveying hose with a conveying pressure.
- the conveyor hose is connected to a conveyor (so-called cleaning machine).
- the conveyor has a compressor.
- the compressed air generated by this is fed to the application nozzle device via a compressed air line running parallel to the delivery hose.
- the wet paste-like mass eg thermal insulation plaster
- the increased pressure that builds up in the compressed air line when it is shut off causes the material feed unit of the cleaning machine to switch off due to feedback to the compressor.
- this machine is equipped with appropriate automatically working and responsive devices.
- the compressed air line is reopened, the increased pressure drops, whereupon the conveyor unit of the cleaning machine for conveying the material is switched on again.
- a spray head for a cleaning machine in which an air-guiding line ends within the same in the flow direction before the application opening of the spray head.
- the plaster is mixed with air within the spray head via this line, so that a plaster / air mixture is dispensed through the application opening.
- a pneumatic shut-off device for the spray head is connected to the air-carrying line.
- a manually operable valve is arranged between the end of the air-carrying line and the shut-off device. When the valve is closed, the shut-off device is closed via the non-escaping compressed air, so that the flow of cleaning material is interrupted.
- application nozzle devices which are provided with a shut-off device in the form of a pinch valve for shutting off the material flow, which essentially consists of a flexible compressible
- a shut-off device in the form of a pinch valve for shutting off the material flow
- a piece of hose through which pasty material (thermal insulation plaster) is conveyed.
- the compressed air can be deflected within the application nozzle device in such a way that it is directed from the outside onto the flexible piece of hose of the pinch valve.
- the flexible hose compresses, its inner surfaces abutting one another and the flow of material interrupted.
- the compressed air control device is set in such a way that the compressed air no longer acts on the pinch valve and is directed in the direction of the material flow, with which pasty material can escape from the application nozzle device.
- the invention has for its object to provide an application device for pasty material, in which the surface to be provided with the application material is automatically cleaned before and / or while the material is being applied.
- the compressed air flows out through an opening which is separate from the application opening of the application nozzle device, namely the outlet of the outflow line.
- the outflow line ends in the vicinity of the application opening of the application nozzle device and is arranged relative to it in such a way that when the surface to be processed is passed with the application nozzle device, compressed air is blown through the outflow line onto the surface before and / or while the paste is being applied to the surface from the application opening Material is applied.
- the compressed air is expediently directed exclusively at the shut-off device by means of the control device or can be discharged via the outflow line while relieving the load on the shut-off device.
- the shut-off device is advantageously designed as a compressed air operated valve which only locks when it is loaded with compressed air and opens automatically at the moment when it is relieved of compressed air.
- a pinch valve of the type described above is conveniently used.
- the outflow line viewed in the direction of movement of the application nozzle device, ends before its application opening, the end of the outflow opening being at an acute angle to the direction of movement of the application nozzle device. Because of this arrangement of the outflow line and its outlet opening, the contaminants of the surface to be processed are blown away in one direction.
- the end of the outflow line is preferably arranged such that its outlet opening is directed away from the application opening of the application nozzle device.
- the arrangement of the discharge line end described here ensures that the dust particles and other loose (foreign) body, the surface to be processed, not in the direction of the application opening, but be blown away by this. This prevents dust particles from being inflated onto material that has already been applied and sticking there.
- both the outflow line and the shut-off device can be connected to a line carrying compressed air or the compressed air source.
- a shut-off valve to be operated by hand is arranged in the outflow line. When the shut-off valve is closed, the shut-off device is pressurized with compressed air and consequently shuts off the material flow. If the shut-off valve is open, the shut-off device is relieved and material emerges from the application nozzle, the compressed air escaping from the outlet opening via the open discharge line.
- the shut-off valve designed as a simple valve thus relieves the shut-off device when it is open.
- the compressed air line is connected to both the shut-off device and the outflow line via a T-connector.
- the outlet opening of the outflow line can be arranged to surround the application opening of the application nozzle device, the compressed air and the pasty material flowing out essentially in mutually parallel directions.
- the outlet opening preferably coaxially surrounds the application opening.
- a conveyor 10 or plastering machine for pasty materials is shown in the overview.
- the conveying device 10 has a unit for conveying the mortar and an integrated compressed air compressor.
- the mortar is transported via a delivery hose 12 to an application nozzle device or processing gun 14.
- the processing gun 14 is connected to the conveyor hose 12 via a compressed air line 16 with the outlet of the compressor of the conveyor 10.
- the pasty adhesive mortar can be applied to a surface 18 to be processed, for example a mineral fiber insulation board 18.
- processing gun 14 The more precise construction of the processing gun 14 is described below with reference to FIGS. 2 and 3 described.
- the processing gun 14 is essentially tubular and has an inlet end 20 to which the delivery hose 12 is connected.
- the application end 22 of the processing gun 14 consists of a curved tube section, the end of which forms the application opening 24 of the processing gun 14. Due to the design of the application end 22 as a curved tube section, the processing gun 14 can be conveniently held in such a way that the plane of the application opening runs parallel to the mineral fiber insulation board 18 and the application opening faces the mineral fiber insulation board 18 (surface to be processed).
- the compressed air line 16 is connected to a three-way switch valve 26, which is attached to the outside of the processing gun 14 on its side.
- the changeover valve 26 has one connected to the compressed air line 16 Inlet 28 and a first and a second outlet 30,32.
- a compressed air pipeline 34 is connected to the first outlet 30 of the changeover valve 26 and leads laterally into the processing gun 14.
- a compressed air outflow pipeline 36 is connected to the second outlet 32 of the changeover valve 26, the end 40 of the outlet opening 38 being guided into the area of the application opening 24 of the processing gun 14.
- a shut-off device 44 Arranged within the processing gun 14 is a shut-off device 44 through which the adhesive mortar can flow, with a pinch valve, which is indicated in FIG. 2 by dashed lines (hereinafter referred to as pinch valve 44).
- the shut-off device or the pinch valve 44 can be actuated by compressed air and blocks the flow of adhesive mortar material when pressurized with compressed air coming through the pipeline 34.
- the pinch valve 44 has an elastic, flexible hose which is compressed as a result of the pressurized air. In one of the two positions of the actuating lever 42 shown in FIG. 3, the adhesive mortar material flow is therefore shut off. By flipping the actuating lever 42, the pinch valve 44 is relieved of the compressed air and opened, so that adhesive mortar can escape from the processing gun 14 via the application opening 24.
- the inlet end 28 of the changeover valve 26 is fluidly connected to its second outlet 32, so that the compressed air supplied via the compressed air line 16 flows out or out through the outflow line 36 and through its outlet opening 38.
- the outlet opening 38 of the discharge line 36 as the order opening 24 of the processing gun 14 is directed onto the surface 18 to be processed, the compressed air can be used with the processing gun 14 switched on to blow away loose impurities (dust particles and mineral fiber residues) from the surface of the mineral fiber insulation board 18 to be processed.
- the outlet opening 38 of the discharge line 36 is arranged in the direction of movement 46 of the processing gun 14 in front of the application opening 24, which is why that area of the mineral fiber insulation board 18 to which adhesive mortar is applied has been cleaned of loose contaminants immediately beforehand.
- the cleaning pretreatment of the mineral fiber insulation board 18 and the application of adhesive mortar therefore take place in a single processing step, which is why a separate cleaning of the surface 18 by hand, for example by tipping over and tapping off the mineral fiber insulation board 18, can be omitted.
- the plane of the outlet opening 38 for the compressed air runs at an acute angle to the surface 18 to be machined, the outlet opening 38 being directed in the direction of movement 46.
- the compressed air therefore does not flow to the application site of the pasty material, but is directed away from this location, which is why the mechanically adhering impurities do not come into contact with the pasty material that has already been applied.
- FIG. 4 shows a second embodiment of an application device in a side view.
- those parts of this application device that correspond to the parts of the application device according to FIGS. 2 and 3 are the same, provided with the same reference numerals.
- FIGS. 2 and 3 4 also has a tubular application nozzle device 14 (or processing gun), which is equipped with a material flow shut-off device 44 with a pinch valve. While the conveying hose 12 for conveying the pasty mortar adhesive material is connected to the inlet end 20 of the application nozzle device 14, the compressed air-carrying hose 16 is connected to the shut-off device 44 via a T-pipe connection piece 52. At the still free end of the T-pipe connector 52, a manually operated shut-off valve 54 is connected (shown in FIG. 4 in the open position), from which the outflow line 36 runs.
- This outflow line 36 ends in a tubular line piece 56 which is arranged from the outside around the front end 22 of the application nozzle device 14 which has the application opening 24. If the line 16 carries compressed air and the shut-off valve 54 shuts off the outflow line 36, the compressed air loads the shut-off device 44 and its pinch valve (indicated in FIG. 4) is shut off, so that pasty material does not escape from the application opening 24. If the shut-off valve 54 is opened, the compressed air flows through the shut-off line 36 into the tubular line piece 56, specifically into the annular space around the end 22 of the application nozzle device 14 which has the application opening 24. From there it strikes the mineral fiber insulation plate 18, specifically in the area in which mortar material emerging from the application opening 24 hits the plate 18. It has been found in tests that the compressed air leaving the line section 56 blows loose contaminants away from the mineral fiber insulation board 18, shortly before the pasty mortar material is applied.
Landscapes
- Engineering & Computer Science (AREA)
- Architecture (AREA)
- Civil Engineering (AREA)
- Structural Engineering (AREA)
- Coating Apparatus (AREA)
- Nozzles (AREA)
- Manufacturing And Processing Devices For Dough (AREA)
- Lubricants (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
Description
- Die Erfindung betrifft im allgemeinen eine Vorrichtung zum maschinellen Auftragen von pastösem Material, insbesondere eine Verarbeitungspistole zum Auftragen von Klebe- und Armiermörtel auf Mineralfaserdämmplatten, wie z. B. aus DE-A-39 16 319 (vgl. Oberbegriff von Anspruch 1) bekannt.
- Von der Verarbeitung von (mineralischen) Wärmedämmputzen sind Auftragdüsenvorrichtungen bekannt, denen der pastöse Wärmedämmputz über einen Förderschlauch mit einem Förderdruck zugeführt wird. Der Förderschlauch ist an einer Fördereinrichtung (sogenannte Putzmaschine) angeschlossen. Die Fördereinrichtung weist einen Kompressor auf. Die von diesem erzeugte Druckluft wird über eine parallel zum Förderschlauch verlaufende Druckluftleitung der Auftragdüsenvorrichtung zugeführt. Mittels der Druckluft wird die nasse pastöse Masse (z.B. Wärmedämmputz) in Form des Wärmedämmputzes aus der Auftragdüsenvorrichtung heraus beschleunigt und gegen die zu bearbeitende Fläche (Hauswand) geworfen. Der sich beim Absperren der Druckluftleitung in dieser aufbauende erhöhte Druck verursacht durch Rückkopplung mit dem Kompressor, daß sich das Material-Förderaggregat der Putzmaschine abschaltet. Hierzu ist diese Maschine mit entsprechenden automatisch arbeitenden und ansprechenden Einrichtungen versehen. Beim Wiederöffnen der Druckluftleitung fällt der erhöhte Druck ab, woraufhin das Förderaggregat der Putzmaschine zum Fördern des Materials wieder eingeschaltet wird.
- Aus DE-A-39 16 319 ist ein Spritzkopf für eine Putzmaschine bekannt, bei dem in Strömungsrichtung vor der Auftragöffnung des Spritzkopfes innerhalb desselben eine Luft führende Leitung endet. Über diese Leitung wird der Putz innerhalb des Spritzkopfes mit Luft vermischt, so daß ein Putz/Luft-Gemisch über die Auftragöffnung ausgegeben wird. Mit der Luft führenden Leitung ist eine pneumatische Absperrvorrichtung für den Spritzkopf verbunden. Zwischen dem Ende der Luft führenden Leitung und der Absperrvorrichtung ist ein von Hand betätigbares Ventil angeordnet. Bei geschlossenem Ventil wird über die nicht entweichende Druckluft die Absperrvorrichtung geschlossen, so daß der Putzmaterialstrom unterbrochen wird.
- Ferner sind Auftragdüsenvorrichtungen bekannt, die zum Absperren des Materialstromes mit einer Absperrvorrichtung in Form eines Quetschventils versehen sind, das im wesentlichen aus einem flexiblen zusammendrückbaren Schlauchstück besteht, durch das pastöses Material (Wärmedämmputz) gefördert wird. Über eine Druckluft-Steuerungseinrichtung in Form eines manuell betätigbaren Drei-Wege-Ventils kann die Druckluft innerhalb der Auftragdüsenvorrichtung derart umgelenkt werden, daß sie von außen auf das flexible Schlauchstück des Quetschventils gerichtet wird. Als Folge davon drückt sich der flexible Schlauch zusammen, wobei seine Innenflächen aneinanderliegen und der Materialstrom unterbrochen ist. Zum erneuten Auftragen des pastösen Materials auf eine zu bearbeitende Oberfläche wird die Druckluft-Steuerungseinrichtung derart eingestellt, daß die Druckluft das Quetschventil nicht länger beaufschlagt und in Richtung des Materialstromes gerichtet ist, womit pastöses Material aus der Auftragdüsenvorrichtung austreten kann.
- Insbesondere beim Auftragen von pastösem Klebe- und Armiermörtel auf Mineralfaserplatten besteht ein Problem in der Notwendigkeit der Befreiung der Mineralfaserdämmplatten von Staubpartikeln und losen Faserresten vor dem Aufbringen des Mörtels, da derartige Verunreinigungen die Haftung des Mörtels an der Mineralfaserdämmplatte beeinträchtigen. Als Folge davon kann es zu versteckten Baumängeln kommen.
- Der Erfindung liegt die Aufgabe zugrunde, eine Auftragvorrichtung für pastöses Material zu schaffen, bei der die mit dem Auftragmaterial zu versehene Fläche automatisch gereinigt wird, bevor und/oder während das Material aufgebracht wird.
- Diese Aufgabe wird erfindungsgemäss mit einer Vorrichtung gelöst, die die Merkmale des Anspruchs 1 aufweist.
- Nach der Erfindung ist vorgesehen, die Druckluft in Richtung auf die zu bearbeitende Fläche ausströmen zu lassen, wenn sie nicht zum Betätigen der Absperrvorrichtung benötigt wird, was beim Auftragen des Materials auf die zu bearbeitende Fläche der Fall ist. Dabei strömt die Druckluft jedoch über eine von der Auftragöffnung der Auftragdüsenvorrichtung getrennte Öffnung, nämlich dem Auslaß der Abströmleitung, ab. Die Abströmleitung endet in der Nähe der Auftragöffnung der Auftragdüsenvorrichtung und ist relativ zu dieser derart angeordnet, daß beim Überfahren der zu bearbeitenden Fläche mit der Auftragdüsenvorrichtung Druckluft durch die Abströmleitung auf die Fläche geblasen wird, bevor und/oder während auf diese aus der Auftragöffnung das pastöse Material aufgetragen wird. Im Falle des Auftragens von z.B. Klebe- und Armiermörtel auf zur Gebäudewärmedämmung verwendete Mineralfaserdämmplatten sind diese also infolge der Druckluftstromung von Staub und Faserresten befreit, bevor und/oder während der Mörtel aufgebracht wird. Ein separates Reinigen der Mineralfaserdämmplatten durch Umkippen und/oder Abklopfen ist nicht mehr erforderlich. Obendrein unterbleibt oftmals unter Zeitdruck diese vorherige gründliche Reinigung der Mineralfaserdämmplatten auf der Baustelle, mit der Folge von (zum Teil versteckten) erheblichen Bauschäden. Die Untergrundbehandlung im Sinne einer Reinigung der mit dem pastösen Material zu versehenen Fläche und der Materialauftrag können also nach dieser Erfindung in einem Arbeitsgang erfolgen. Somit leistet diese Erfindung nicht nur einen ganz wesentlichen Beitrag zur Erleichterung der Verarbeitung der genannten Baumaterialien, sondern trägt zugleich zu einer qualitativen Verbesserung der Bauwerkssicherheit durch Vermeidung der erwähnten Bauschäden bei.
- Zweckmäßigerweise ist die Druckluft mittels der Steuerungsvorrichtung entweder ausschließlich auf die Absperrvorrichtung gerichtet oder unter Entlastung der Absperrvorrichtung über die Abströmleitung abführbar.
- Die Absperrvorrichtung ist vorteilhafterweise als ein druckluftbetriebenes Ventil ausgebildet, das nur dann, wenn es druckluftbelastet ist, sperrt und in dem Augenblick, in dem es druckluftentlastet ist, automatisch öffnet. Praktischerweise wird ein Quetschventil der zuvor beschriebenen Art eingesetzt.
- In vorteilhafter Weiterbildung der Erfindung ist vorgesehen, daß die Abströmleitung in Bewegungsrichtung der Auftragdüsenvorrichtung betrachtet vor deren Auftragöffnung endet, wobei das Ende der Abströmöffnung in einem spitzen Winkel zur Bewegungsrichtung der Auftragdüsenvorrichtungverläuft. Aufgrund dieser Anordnung der Abströmleitung und dessen Auslaßöffnung werden die Verunreinigungen der zu bearbeitenden Fläche zu einer Richtung hin weggeblasen. Vorzugsweise ist das Ende der Abströmleitung derart angeordnet, daß deren Auslaßöffnung von der Auftragöffnung der Auftragdüsenvorrichtung weg gerichtet ist. Bei entsprechender Bewegung der Auftragdüsenvorrichtung über die zu bearbeitende Fläche zwecks Auftragen des pastösen Materials wird durch die hier beschriebene Anordnung des Abströmleitungsendes erreicht, daß die Staubpartikel und sonstigen losen (Fremd-)Körper, der zu bearbeitenden Fläche, nicht in Richtung auf die Auftragöffnung, sondern von dieser weg geblasen werden. Damit wird verhindert, daß Staubpartikel auf bereits aufgetragenes Material aufgeblasen werden und dort haften bleiben.
- In vorteilhafter Weiterbildung der Erfindung sind sowohl die Abströmleitung als auch die Absperrvorrichtung mit einerdruckluftführenden Leitung bzw. der Durckluftquelle verbindbar. In der Abströmleitung ist ein von Hand zu bedienendes Absperrventil angeordnet. Bei geschlossenem Absperrventil wird die Absperrvorrichtung mit Druckluft beaufschlagt und sperrt infolgedessen den Materialstrom ab. Ist das Absperrventil geöffnet, so ist die Absperrvorrichtung entlastet und Material tritt aus der Auftragdüse aus, wobei die Druckluft über die offene Abströmleitung aus deren Auslaßöffnung heraus entweicht. Das als einfaches Ventil ausgebildete Absperrventil entlastet also die Absperrvorrichtung, wenn es geöffnet ist. Praktischerweise ist die druckluftführende Leitung über ein T-Verbindungsstück mit sowohl der Absperrvorrichtung als auch der Abströmleitung verbunden. Die Auslaßöffnung der Abströmleitung kann die Auftragöffnung der Auftragdüsenvorrichtung umgebend angeordnet sein, wobei die Druckluft und das pastöse Material im wesentlichen in zueinander parallelen Richtungen ausströmen. Vorzugsweise umgibt die Auslaßöffnung die Auftragöffnung koaxial.
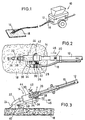
- Nachfolgend werden anhand der Figuren Ausführungsbeispiele der Erfindung näher erläutert. Im einzelnen zeigen:
- Fig. 1
- eine Fördereinrichtung zum Fördern von pastösem Material mit an dieser über einen Förderschlauch angeschlossenen Auftragdüsenvorrichtung,
- Fig. 2
- eine Aufsicht auf eine Auftragdüsenvorrichtung gemäß einem ersten Ausführungsbeispiel,
- Fig. 3
- eine Seitenansicht der Auftragdüsenvorrichtung gemäß Fig. 2 und
- Fig. 4
- in Seitenansicht ein zweites Ausführungsbeispiel einer Auftragdüsenvorrichtung.
- In Fig. 1 ist in der Übersicht eine Fördereinrichtung 10 oder Putzmaschine für pastöse Materialien (Klebe- und Armiermörtel) dargestellt. Die Fördereinrichtung 10 weist ein Aggregat zum Fördern des Mörtels und einen integrierten Druckluft-Kompressor auf. Der Mörtel wird über einen Förderschlauch 12 zu einer Auftragdüsenvorrichtung oder Verarbeitungspistole 14 transportiert. Die Verarbeitungspistole 14 ist neben dem Förderschlauch 12 über eine Druckluftleitung 16 mit dem Auslaß des Kompressors der Fördereinrichtung 10 verbunden. Mit Hilfe der Verarbeitungspistole 14 läßt sich der pastöse Klebemörtel auf eine zu bearbeitende Oberfläche 18, beispielsweise eine Mineralfaserdämmplatte 18 auftragen.
- Der genauere Aufbau der Verarbeitungspistole 14 wird nachfolgend anhand der Fign. 2 und 3 beschrieben.
- Die Verarbeitungspistole 14 ist im wesentlichen rohrförmig ausgebildet und weist ein Einlaßende 20 auf, an dem der Förderschlauch 12 angeschlossen ist. Das Auftragende 22 der Verarbeitungspistole 14 besteht aus einem gekrümmten Rohrabschnitt, dessen Ende die Auftragöffnung 24 der Verarbeitungspistole 14 bildet. Aufgrund der Ausbildung des Auftragendes 22 als gekrümmter Rohrabschnitt läßt sich die Verarbeitungspistole 14 bequem derart halten, daß die Ebene der Auftragöffnung parallel zur Mineralfaserdämmplatte 18 verläuft und die Auftragöffnung zur Mineralfaserdämmplatte 18 (zu bearbeitenden Oberfläche) weist.
- Die Druckluftleitung 16 ist an einem Drei-Wege-Umschaltventil 26 angeschlossen, das außen an der Verarbeitungspistole 14 zu dessen Seite angebracht ist. Das Umschaltventil 26 weist einen mit der Druckluftleitung 16 verbundenen Einlaß 28 sowie einen ersten und einen zweiten Auslaß 30,32 auf. An dem ersten Auslaß 30 des Umschaltventils 26 ist eine Druckluft-Rohrleitung 34 angeschlossen, die seitlich in die Verarbeitungspistole 14 hineinführt. An dem zweiten Auslaß 32 des Umschaltventils 26 ist eine Druckluft-Abströmrohrleitung 36 angeschlossen, deren die Auslaßöffnung 38 aufweisendes Ende 40 bis in den Bereich der Auftragöffnung 24 der Verarbeitungspistole 14 geführt ist. Durch Verschwenkung eines Betätigungshebels 42 läßt sich das Umschaltventil 26 derart einstellen, daß der Einlaß 28 entweder mit dem ersten Auslaß 30 oder mit dem zweiten Auslaß 32 strömungsmäßig verbunden ist.
- Innerhalb der Verarbeitungspistole 14 ist eine von dem Klebemörtel durchströmbare Absperrvorrichtung 44 mit einem Quetschventil angeordnet, das in Fig. 2 durch gestrichelte Linien angedeutet ist (nachfolgend mit Quetschventil 44 bezeichnet). Die Absperrvorrichtung bzw. das Quetschventil 44 ist druckluftbetätigbar und sperrt bei Beaufschlagung mit über die Rohrleitung 34 anstehender Druckluft den Klebemörtel-Materialfluß ab. Das Quetschventil 44 weist einen elastischen flexiblen Schlauch auf, der infolge der Druckluftbeaufschlagung zugedrückt wird. In einer der beiden in Fig. 3 dargestellten Stellungen des Betätigungshebels 42 wird also der Klebemörtel-Materialstrom abgesperrt. Durch Umlegen des Betätigungshebels 42 wird das Quetschventil 44 von der Druckluft entlastet und geöffnet, so daß über die Auftragöffnung 24 Klebemörtel aus der Verarbeitungspistole 14 austreten kann. Hierbei ist das Einlaßende 28 des Umschaltventils 26 mit dessen zweitem Auslaß 32 strömungsmäßig verbunden, so daß die über die Druckluftleitung 16 zugeführte Druckluft durch die Abströmleitung 36 und über deren Auslaßöffnung 38 ab- bzw. ausströmt. Da die Auslaßöffnung 38 der Abströmleitung 36 wie die Auftragöffnung 24 der Verarbeitungspistole 14 auf die zu bearbeitende Oberfläche 18 gerichtet ist, kann die Druckluft bei eingeschalteter Verarbeitungspistole 14 zum Wegblasen von losen Verunreinigungen (Staubpartikeln und Mineralfaserresten) von der zu bearbeitenden Oberfläche der Mineralfaserdämmplatte 18 verwendet werden. Wie anhand von Fig. 3 zu erkennen ist, ist die Auslaßöffnung 38 der Abströmleitung 36 in Bewegungsrichtung 46 der Verarbeitungspistole 14 vor der Auftragöffnung 24 angeordnet, weshalb derjenige Bereich der Mineralfaserdämmplatte 18, auf den Klebemörtel aufgebracht wird, unmittelbar zuvor von losen Verunreinigungen gereinigt ist. Die Reinigungsvorbehandlung der Mineralfaserdämmplatte 18 und das Auftragen von Klebemörtel erfolgen also in einem einzigen Verarbeitungsschritt, weshalb ein separates Reinigen der Oberfläche 18 von Hand durch beispielsweise Umkippen und Abklopfen der Mineralfaserdämmplatte 18 unterbleiben kann.
- Wie in Fig. 3 angedeutet, verläuft die Ebene der Auslaßöffnung 38 für die Druckluft in einem spitzen Winkel zur zu bearbeitenden Oberfläche 18, wobei die Auslaßöffnung 38 in Bewegungsrichtung 46 gerichtet ist. Die Druckluft strömt also nicht zur Auftragstelle des pastösen Materials, sondern ist von dieser Stelle weggerichtet, weshalb die mechanisch anhaftenden Verunreinigungen nicht in Berührung mit bereits aufgetragenem pastösen Material gelangen.
- In Fig. 4 ist ein zweites Ausführungsbeispiel einer Auftragvorrichtung in Seitenansicht dargestellt. Soweit möglich, sind diejenigen Teile dieser Auftragvorrichtung, die den Teilen der Auftragvorrichtung gemäß Fign. 2 und 3 gleichen, mit den gleichen Bezugszeichen versehen.
- Wie bei dem Ausführungsbeispiel gemäß den Fign. 2 und 3 weist auch die Auftragvorrichtung 50 gemäß Fig. 4 eine rohrförmige Auftragdüsenvorrichtung 14 (oder Verarbeitungspistole) auf, die mit einer Materialfluß-Absperrvorrichtung 44 mit Quetschventil ausgestattet ist. Während der Förderschlauch 12 zum Fördern des pastösen Mörtelklebermaterials an dem Einlaßende 20 der Auftragdüsenvorrichtung 14 angeschlossen ist, ist der druckluftführende Schlauch 16 über ein T-Rohrverbindungsstück 52 mit der Absperrvorrichtung 44 verbunden. An dem noch freien Ende des T-Rohrverbindungsstückes 52 ist ein von Hand zu bedienendes Absperrventil 54 angeschlossen (in Fig. 4 in Öffnungsstellung gezeigt), von dem aus die Abströmleitung 36 verläuft. Diese Abströmleitung 36 endet in einem rohrförmigen Leitungsstück 56, das von außen um das die Auftragöffnung 24 aufweisende vordere Ende 22 der Auftragdüsenvorrichtung 14 herum angeordent ist. Sofern die Leitung 16 Druckluft führt und das Absperrventil 54 die Abströmleitung 36 absperrt, belastet die Druckluft die Absperrvorrichtung 44 und deren Quetschventil (in Fig. 4 angedeutet) ist abgesperrt, so daß aus der Auftragöffnung 24 pastöses Material nicht austritt. Wird das Absperrventil 54 geöffnet, so strömt die Druckluft durch die Absperrleitung 36 in das rohrförmige Leitungsstück 56, und zwar in den Ringraum um das die Auftragöffnung 24 aufweisende Ende 22 der Auftragdüsenvorrichtung 14. Von dort aus trifft es auf die Mineralfaserdämmplatte 18 auf und zwar in demjenigen Bereich, in dem auf die Platte 18 gerade aus der Auftragöffnung 24 austretendes Mörtelmaterial auftrifft. Es hat sich bei Versuchen herausgestellt, daß die das Leitungsstück 56 verlassende Druckluft lose Verunreinigungen von der Mineralfaserdämmplatte 18 wegbläst, und zwar kurz bevor das pastöse Mörtelmaterial aufgebracht wird.
Claims (8)
- Vorrichtung zum maschinellen Auftragen von pastösem Material auf eine zu bearbeitende Fläche, insbesondere zum Auftragen von Klebe- und Armiermörtel auf Mineralfaserdämmplatten, mit- einer Auftragdüsenvorrichtung (14), die an einen Förderschlauch (12) zum Transportieren des unter einem Förderdruck stehenden pastösen Materials anschließbar ist und eine Auftragöffnung (24) zum Austreten des pastösen Materials aufweist,- einer druckluftbetriebenen Absperrvorrichtung (44) zum Unterbinden des Austritts von pastösem Material bei auf die Absperrvorrichtung (44) wirkender Druckluft und- einer Druckluft-Steuerungseinrichtung (26;54) zum wahlweisen Richten der Druckluft entweder auf die Absperrvorrichtung (44) zwecks Unterbindung des Austritts von pastösem Material aus der Auftragdüsenvorrichtung (14) oder in eine Abströmleitung (36), die eine Auslaßöffnung (38) aufweist, welche wie die Auftragöffnung (24) der Auftragdüsenvorrichtung (14) auf die zu bearbeitende Fläche gerichtet ist,dadurch gekennzeichnet,
daß die Auslaßöffnung (38) der Abströmleitung (36) und die Auftragöffnung (24) der Auftragdüsenvorrichtung (14) derart relativ zueinander angeordnet sind, daß die Druckluft und das pastöse Material getrennt voneinander ausströmen. - Vorrichtung nach Anspruch 1, dadurch gekennzeichnet, daß die Druckluft-Steuerungseinrichtung (26) ein manuell betätigbares Umschaltventil mit einem Einlaß (28) und zwei Auslässen (30,32) aufweist, wobei an den Einlaß (28) eine Druckluft führende Leitung (16) anschließbar ist, und daß der eine Auslaß (30) des Umschaltventils (26) mit der Absperrvorrichtung (44) und der andere Auslaß (32) mit der Abströmleitung (36) verbunden ist.
- Vorrichtung nach Anspruch 1, dadurch gekennzeichnet, daß die Druckluft-Steuerungseinrichtung ein manuell betätigbares Absperrventil (54) aufweist, das in der Abströmleitung (36) angeordnet ist, und daß die Abströmleitung (36) und die Absperrvorrichtung (44) mit einer druckluftführenden Leitung (16) verbunden ist.
- Vorrichtung nach einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, daß die Abströmleitung (36) in Bewegungsrichtung (46) der Auftragdüsenvorrichtung (14) betrachtet vor deren Auftragöffnung (24) endet, wobei die Auslaßöffnung (38) in einem spitzen Winkel zur Bewegungsrichtung der Auftragdüsenvorrichtung (14) gerichtet ist.
- Vorrichtung nach einem der Ansprüche 1 bis 4, dadurch gekennzeichnet, daß das Ende (40) der Abströmleitung (36) derart angeordnet ist, daß deren Auslaßöffnung (38) von der Auftragöffnung (24) der Auftragdüsenvorrichtung (14) weg gerichtet ist.
- Vorrichtung nach einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, daß die Auslaßöffnung der Abströmleitung die Auftragöffnung der Auftragdüsenvorrichtung umgibt.
- Vorrichtung nach Anspruch 6, dadurch gekennzeichnet, daß die Auslaßöffnung der Abströmleitung die Auftragöffnung der Auftragdüsenvorrichtung koaxial umgibt.
- Vorrichtung nach einem der Ansprüche 1 bis 7, dadurch gekennzeichnet, daß die Druckluft mittels der Steuerungsvorrichtung (26; 54) entweder ausschließlich auf die Absperrvorrichtung (44) gerichtet ist oder unter Entlastung der Absperrvorrichtung (44) über die Abströmleitung (36) abführbar ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE4320819A DE4320819C2 (de) | 1993-06-23 | 1993-06-23 | Vorrichtung zum maschinellen Auftragen von pastösem Material auf eine zu bearbeitende Fläche |
| DE4320819 | 1993-06-23 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0631822A1 EP0631822A1 (de) | 1995-01-04 |
| EP0631822B1 true EP0631822B1 (de) | 1997-01-08 |
Family
ID=6490999
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP94104125A Expired - Lifetime EP0631822B1 (de) | 1993-06-23 | 1994-03-16 | Vorrichtung zum maschinellen Auftragen von pastösem Material auf eine zu bearbeitende Fläche |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0631822B1 (de) |
| AT (1) | ATE147287T1 (de) |
| DE (2) | DE4320819C2 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AU2006206758B2 (en) * | 2005-01-18 | 2010-09-16 | Apla-Tech, Inc. | Material management system for continuous flow of drywall compound |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| SE422427B (sv) * | 1977-10-17 | 1982-03-08 | Bertil Sandell | Sett att tillverka fiberarmerade byggnadskonstruktioner, ytbeleggningar och dylikt samt anordning for genomforande av settet |
| DE3916319A1 (de) * | 1989-05-19 | 1990-11-29 | Harry Reinhardt | Spritzkopf an einer putzmaschine |
| US4961537A (en) * | 1989-09-28 | 1990-10-09 | Djs & T Limited Partnership | Pressure operated spray applicator |
| DE9011215U1 (de) * | 1990-07-31 | 1990-10-31 | Grude GmbH Ingenieurbüro, 2000 Hamburg | Farbspritzpistole für Heißplastik- Straßenmarkierung |
-
1993
- 1993-06-23 DE DE4320819A patent/DE4320819C2/de not_active Expired - Fee Related
-
1994
- 1994-03-16 DE DE59401508T patent/DE59401508D1/de not_active Expired - Fee Related
- 1994-03-16 AT AT94104125T patent/ATE147287T1/de active
- 1994-03-16 EP EP94104125A patent/EP0631822B1/de not_active Expired - Lifetime
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AU2006206758B2 (en) * | 2005-01-18 | 2010-09-16 | Apla-Tech, Inc. | Material management system for continuous flow of drywall compound |
Also Published As
| Publication number | Publication date |
|---|---|
| DE4320819C2 (de) | 1997-01-30 |
| DE59401508D1 (de) | 1997-02-20 |
| ATE147287T1 (de) | 1997-01-15 |
| EP0631822A1 (de) | 1995-01-04 |
| DE4320819A1 (de) | 1995-01-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2524156A1 (de) | Strahlgeraet zum spritzen koernigen guts | |
| DE2245538C3 (de) | Förderband-Waschanlage | |
| EP0009660A1 (de) | Verfahren und Vorrichtung zum Spritzen von Beton | |
| DE19812275B4 (de) | Transportvorrichtung | |
| DE2150331A1 (de) | Verfahren und Vorrichtung zur Reinigung von Spinnkammern | |
| CH659644A5 (de) | Verfahren und vorrichtung zum knotenfreien verbinden zweier faeden. | |
| DE69201220T2 (de) | Elektrostatische Farbspritzanlage für Pulverbeschichtungsmaterial. | |
| DE4320819C2 (de) | Vorrichtung zum maschinellen Auftragen von pastösem Material auf eine zu bearbeitende Fläche | |
| DE4402568A1 (de) | Verfahren und Vorrichtung zum Eintragen von granulatförmigen Dämmaterialien an Baustellen | |
| DE4114097A1 (de) | Vorrichtung zur pulverbeschichtung | |
| DE3413576A1 (de) | Verfahren und geraet zum abstrahlen von werkstuecken, bauwerken u.dgl. mittels eines mit einem koernigen strahlmittel beladenen traegerluftstromes | |
| AT405047B (de) | Vorrichtung zum unterteilen einer papierbahn | |
| EP0542212B1 (de) | Vorrichtung zum Reinigen von Rohren | |
| DE69716693T2 (de) | Steuerungsvorrichtung für eine Reinigungsvorrichtung für verseuchte Oberflächen | |
| DE4319266C2 (de) | Spleißvorrichtung | |
| DE19701010A1 (de) | Verfahren zur Sanierung der Innenwände festverlegter Rohrleitungen | |
| DE3214764A1 (de) | Vorrichtung zum strahlen feinwerktechnischer werkstuecke | |
| DE3330892A1 (de) | Vorrichtung zum spritzen von beton, moertel oder feuerfesten auskleidungsmaterialien | |
| DE3232994A1 (de) | Schleuderstrahlmaschine | |
| EP1361941B1 (de) | Verfahren zum abtragen einer äusseren schicht eines mauerwerkes und vorrichtung zum entfernen der äusseren schicht, insbesondere von fugenmörtel | |
| DE9105321U1 (de) | Vorrichtung zur Pulverbeschichtung | |
| DE4407956A1 (de) | Sandstrahlkasten zur Oberflächenbehandlung von vorzugsweise flachen Materialoberflächen | |
| WO1998024592A1 (de) | Einrichtung zum strahlen mit trockenem und feuchtem strahlmittel | |
| AT403316B (de) | Einrichtung zum unterbrechen eines materialflusses in einem elastisch verformbaren schlauch | |
| DE2738234C2 (de) | Verfahren und Vorrichtung zum Versetzen von Mineralwollefasern, insbesondere von Schlackenwollefasern, mit einem pulverförmigen Bindemittel |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT CH DE FR LI |
|
| 17P | Request for examination filed |
Effective date: 19950310 |
|
| 17Q | First examination report despatched |
Effective date: 19950529 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT CH DE FR LI |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19970108 |
|
| REF | Corresponds to: |
Ref document number: 147287 Country of ref document: AT Date of ref document: 19970115 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 59401508 Country of ref document: DE Date of ref document: 19970220 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19970316 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19970331 Ref country code: CH Effective date: 19970331 |
|
| EN | Fr: translation not filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20070530 Year of fee payment: 14 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081001 |