EP0600324A1 - Verfahren zur Unterdruck-Herstellung bei einer Druckgiessmaschine - Google Patents
Verfahren zur Unterdruck-Herstellung bei einer Druckgiessmaschine Download PDFInfo
- Publication number
- EP0600324A1 EP0600324A1 EP93118695A EP93118695A EP0600324A1 EP 0600324 A1 EP0600324 A1 EP 0600324A1 EP 93118695 A EP93118695 A EP 93118695A EP 93118695 A EP93118695 A EP 93118695A EP 0600324 A1 EP0600324 A1 EP 0600324A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- vacuum
- casting
- negative pressure
- casting chamber
- pressure
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000034 method Methods 0.000 title claims abstract description 27
- 238000004512 die casting Methods 0.000 title claims abstract description 19
- 238000005266 casting Methods 0.000 claims abstract description 72
- 239000000523 sample Substances 0.000 claims abstract description 5
- 229910052751 metal Inorganic materials 0.000 claims description 17
- 239000002184 metal Substances 0.000 claims description 17
- 239000000155 melt Substances 0.000 claims description 12
- 230000001105 regulatory effect Effects 0.000 claims description 7
- 239000007789 gas Substances 0.000 claims description 6
- 238000010792 warming Methods 0.000 claims description 4
- 238000007872 degassing Methods 0.000 claims description 3
- 238000001514 detection method Methods 0.000 claims description 2
- 238000006073 displacement reaction Methods 0.000 claims description 2
- 238000010943 off-gassing Methods 0.000 claims description 2
- 230000000750 progressive effect Effects 0.000 claims description 2
- 229910045601 alloy Inorganic materials 0.000 claims 1
- 239000000956 alloy Substances 0.000 claims 1
- 230000001276 controlling effect Effects 0.000 claims 1
- 238000002844 melting Methods 0.000 claims 1
- 230000008018 melting Effects 0.000 claims 1
- 150000002739 metals Chemical class 0.000 claims 1
- 239000011148 porous material Substances 0.000 claims 1
- 238000005259 measurement Methods 0.000 abstract description 2
- 238000011161 development Methods 0.000 description 2
- 230000018109 developmental process Effects 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 238000007792 addition Methods 0.000 description 1
- 230000000903 blocking effect Effects 0.000 description 1
- 238000011156 evaluation Methods 0.000 description 1
- 238000001595 flow curve Methods 0.000 description 1
- 239000012535 impurity Substances 0.000 description 1
- 229910001338 liquidmetal Inorganic materials 0.000 description 1
- 230000000149 penetrating effect Effects 0.000 description 1
- 230000035515 penetration Effects 0.000 description 1
- 230000002028 premature Effects 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D17/00—Pressure die casting or injection die casting, i.e. casting in which the metal is forced into a mould under high pressure
- B22D17/14—Machines with evacuated die cavity
- B22D17/145—Venting means therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D17/00—Pressure die casting or injection die casting, i.e. casting in which the metal is forced into a mould under high pressure
- B22D17/20—Accessories: Details
- B22D17/32—Controlling equipment
Definitions
- the invention relates to a method for producing the negative pressure in a die casting machine, in particular a vacuum die casting machine according to the preamble of claim 1.
- the negative pressure (vacuum) applied to the casting mold can be effective until the casting mold is filled with liquid metal by the advancing movement of the casting piston, a valve with a hydraulically actuated blocking piston being located on the casting mold and preventing the metal melt from penetrating into the Suction channel prevented.
- the method according to the invention with the characterizing features of claim 1 aims and achieves a considerable improvement in the evacuation of the air, in particular in the known vacuum pressure casting method.
- the method can also be used in the normal pressure casting process for evacuating the air.
- the invention is based on the main idea that the vacuum applied not only in terms of its size, i. H. with regard to the negative pressure produced and with regard to the duty cycle, but the vacuum can moreover be precisely adapted to the respective conditions of the die casting process.
- This is done according to the invention by regulating the vacuum over the period of time of the application of negative pressure, ie. H.
- the size and duration of the vacuum applied is subjected to the most precise control.
- the inlet of the melt through the suction pipe into the casting chamber and into the casting mold can be regulated at any time, so that - if necessary in conjunction with further auxiliary measures - an optimal filling of both the casting chamber and an optimal casting process can be achieved during the casting process itself .
- Turbulence in the metal flow can also be avoided. Basically, an optimal degassing of the metal is achieved. Through continuous regulation or control of the absolute pressure of the vacuum during the casting process, considerable improvements in the die-cast products are achieved. According to the invention, a precise regulation of the vacuum with regard to an undesired premature entry of the molten metal into the mold cavity during the filling of the casting chamber is in particular avoided, which leads to undesirable flow marks on the casting.
- the invention is described using a vacuum die casting machine. It can also be used for the "evacuation" of normal die casting machines if the casting piston has closed the filling opening.
- Fig. 1 the fixed platen 2 is shown with a fixed mold half 3, which cooperates with the movable mold half 4 of a die casting machine 1 only indicated.
- the mold cavity 5, which is to be filled with molten metal, is located between the fixed 3 and the movable mold half 4.
- a casting chamber 6 with a casting piston 7 is provided, into which the molten metal 8 is drawn in from a holding device 10 via a suction pipe 9.
- the molten metal is not sucked out of the holding device 10 by a casting process, but rather by applying a vacuum or negative pressure.
- the suction process takes place through the suction pipe 9 via the casting chamber 6 and the mold cavity 5.
- a vacuum valve 11 with a vacuum connection line 12 on the mold halves 3, 4, which leads to a switching valve 13.
- the vacuum line 12 is continued from the switching valve 13 to a vacuum tank 14, to which a vacuum pump 15 is connected to produce the negative pressure.
- the vacuum valve 11 of the casting mold serves to shut off the metal melt, which may be pressed in up to this location by means of the casting piston 7. Penetration of the metal into the subsequent vacuum connection line 12 is thus avoided.
- the vacuum applied via the vacuum valve 11 is regulated via the switching valve 13 in its pressure profile such that the pressure in the mold cavity 5, in the casting chamber 6 and in the suction pipe 9 is regulated according to a certain adjustable function per unit of time.
- a computer 16 is provided, which records a wide variety of parameters.
- the negative pressure in the area of the vacuum valve 11 is detected via an additional measuring line 17 and measured by means of a vacuum measuring probe.
- This vacuum measuring probe 18 is connected to the vacuum connecting line 12 via an additional shunt valve 19.
- the pressure p in the vacuum connecting line 12 can thus be detected and fed to the computer 16 via the line 20.
- the vacuum pressure in the system can also be supplied to the computer 16 via other measuring lines in the system. This is indicated, for example, by a measuring line 21 to the vacuum tank 14.
- the pressure curve or mass flow curve set over time can be a progressive, take a linear or degressive course.
- the switching valve 13 in the vacuum connecting line is controlled via the computer 16, for example via the control line 22, in such a way that the desired pressure profile or mass flow profile is established in the vacuum line 12.
- the computer 16 can control the vacuum valve 11 via a control line 23 and control the shunt valve 19 via a further control line 24.
- the production of the vacuum itself ie the operation of the vacuum pump 15, can also take place via a further control line 25.
- the melt 8 is absolutely sucked out of the warming device 10 via a throttle 30 located at the lower end of the suction pipe 9 into the casting chamber 6 by applying a high negative pressure of the order of p1 ⁇ 150 to 200 mbar.
- the size of the throttle 30, the intake time t 1 and the negative pressure p 1 determines the amount m 1 of the molten metal that is sucked into the casting chamber.
- An additional sensor z. B. an ultrasonic sensor 28 in the upper wall of the casting chamber or a resistance sensor 28 'in the sprue cross section of the mold half 4 can detect the fill level h 1 in the casting chamber 6 and supply this value via a measuring line 29 to the computer 16 for evaluation.
- the suction process in vacuum pressure casting machines can be ended as the first control section by passing over the casting piston 7 via the suction or inlet opening 27 into the casting chamber 6 or by a correspondingly reduced negative pressure (pressure increase). It corresponds to the process of filling molten metal into a "normal" Die casting device.
- the position of the casting piston 7 can be fed to the computer 16 via a line 32 via a travel detection sensor 31, in order to detect the piston position after passing over the filling opening 27 and to regulate the vacuum, particularly in "normal” casting chambers.
- Sensors for detecting the path or the fill level are known per se (see, e.g., Maschinen mod 1992, 40, pages 72-77).
- This first filling period t 1 is followed by a further "holding period” t 2.
- a certain holding time of the vacuum of t2 ⁇ 0.2 to 3 seconds is set over a period of time t2 after a continuous drop in the vacuum (pressure increase) to a vacuum of preferably p2 ⁇ 800 mbar absolute.
- This holding time can be measured depending on the specific metal weight, the suction pipe height h2 or the fill level h1 in the casting chamber and the shape of the mold.
- the invention further provides that in the first output phase t1 when the melt 8 passes from the suction pipe 9 into the casting chamber 6 at the inlet opening 27 of the casting chamber, a constant melt speed v ⁇ 1 m / sec can be set due to the controllable low pressure, flow values preferably on the order of less than 1 m / sec.
- the casting piston 7 is provided in its lower region with a deflection surface 26, as is the case in the applicant's prior publication according to DE 41 01 592 is described.
- the casting mold is filled in a manner known per se by the displacement of the piston 7 in the casting chamber 6 in a pre-filling and mold-filling phase.
- the regulation of the negative pressure over this third time period t 3 serves to extract the remaining air or gas components.
- the invention is not restricted to the exemplary embodiment shown and described. Rather, it also includes all professional developments and additions within the framework of the inventive concept.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
- Casting Or Compression Moulding Of Plastics Or The Like (AREA)
Abstract
Description
- Die Erfindung betrifft ein Verfahren zur Herstellung des Unterdrucks bei einer Druckgießmaschine insbesondere einer Vakuum-Druckgießmaschine nach dem Oberbegriff des Anspruchs 1.
- Aus der EP 0 051 310 B1 ist eine Druckgießmaschine bekanntgeworden, die nach dem sogenannten Vakuum-Druckgießverfahren arbeitet. Bei diesem Verfahren wird die Metallschmelze aus einem Warmhalteofen über ein Ansaugrohr in die Gießkammer mittels Unterdruck angesaugt, wobei der Unterdruck über einen Absaugkanal in der Formteilungsfläche der Gießform aufgebracht wird. Wie in der zitierten Literaturstelle weiterhin beschrieben, stellt sich bei Druckgießmaschinen auch das Problem einer ausreichenden Entgasung der Schmelze während des Gießvorganges dar. Zwar wird durch Anwendung des Vakuum-Druckgießverfahrens eine Verbesserung durch ein Absaugen der im Saugrohr, in der Gießkammer sowie in der Gießform enthaltenen Gase erzielt. Versuche haben jedoch gezeigt, daß aufgrund von vorhandenem Restgas und von Verwirbelungen der Schmelze sowie sonstigen Verunreinigungen noch erhebliche Qualitätseinbußen hinzunehmen sind. Um eine Verbesserung zu erzielen, wurden in den in der oben genannten Literaturstelle weiterhin zitierten Veröffentlichungen vorgeschlagen, mehrere Vakuumanschlüsse zur Verbesserung der Evakuierung vorzusehen. Insbesondere schlägt diese zitierte Literaturstelle selbst vor, einen weiteren Vakuumanschluß durch den Gießkolben selbst vorzunehmen.
- Der an die Gießform angelegte Unterdruck (Vakuum) kann so lange wirksam sein, bis die Gießform durch die Vorschubbewegung des Gießkolbens mit flüssigem Metall gefüllt ist, wobei sich an der Gießform ein Ventil mit einem hydraulisch betätigbaren Sperrkolben befindet, der ein Eindringen der Metallschmelze in den Absaugkanal verhindert.
- Aus der Literaturstelle "Gießerei" 69 (1982) Heft 19, Seite 521/527 wird bei einem derartigen Gießverfahren darauf hingewiesen, daß die Zeitdauer des angelegten Vakuums von Bedeutung ist. Die Vakuumeinwirkzeit ist neben der Größe des eingestellten Unterdrucks demnach ein wichtiger Parameter, um eine richtige und effektive Evakuierung der einzelnen Teile, nämlich Saugrohr, Gießkammer und Druckgießform zu erzielen.
- Das erfindungsgemäße Verfahren mit den kennzeichnenden Merkmalen des Anspruchs 1 bezweckt und erreicht eine erhebliche Verbesserung beim Evakuieren der Luft insbesondere beim bekannten Vakuum-Druckgießverfahren. Das Verfahren kann auch beim normalen Druckgußverfahren zur Evakuierung der Luft angewandt werden.
- Der Erfindung liegt der Kerngedanke zugrunde, daß das angelegte Vakuum nicht nur hinsichtlich seiner Größe, d. h. hinsichtlich des hergestellten Unterdrucks sowie hinsichtlich der Einschaltdauer berücksichtigt wird, sondern das Vakuum kann darüber hinaus den jeweiligen Bedingungen des Druckgießverfahrens genauestens angepaßt werden. Dies geschieht erfindungsgemäß durch eine Regelung des Vakuums über die Zeitdauer der Unterdruckbeaufschlagung, d. h. das angelegte Vakuum wird in seiner Größe sowie seiner Zeitdauer einer genauesten Regelung unterworfen. Hierdurch kann auch der Einlauf der Schmelze über das Saugrohr in die Gießkammer und in die Gießform zu jedem Zeitpunkt reguliert werden, so daß - gegebenenfalls in Verbindung mit weiteren Hilfsmaßnahmen - eine optimale Befüllung sowohl der Gießkammer als auch ein optimaler Gießprozeß beim Gießvorgang selbst erzielt werden kann. Weiterhin können Turbulenzen der Metallströmung vermieden werden. Grundsätzlich wird eine optimale Entgasung des Metalls erzielt. Durch eine kontinuierliche Regelung oder Steuerung des absoluten Druckes des Vakuums während des Gießprozesses werden damit erhebliche Verbesserungen an den Druckgießerzeugnissen erzielt. Gemäß der Erfindung wird insbesondere auch eine genaue Regulierung des Vakuums im Hinblick auf einen unerwünschten vorzeitigen Eintritt der Metallschmelze in den Formhohlraum während der Gießkammerbefüllung vermieden, was zu unerwünschten Fließspuren auf dem Gußteil führt.
- In den Unteransprüchen sind vorteilhafte und zweckmäßige Weiterbildungen des erfindungsgemäßen Verfahrens angegeben. Besonders vorteilhaft hierbei ist die kontinuierliche oder diskontinuierliche Regelung des Vakuums gegebenenfalls mit Einhaltung von Haltezeiten bei bestimmten Unterdrücken.
- Die Erfindung wird näher am Beispiel einer Vakuum-Druckgießmaschine beschrieben, die in der Zeichnung dargestellt und unter Angabe weiterer Vorteile in der nachfolgenden Beschreibung näher erläutert ist. Es zeigt
- Fig. 1
- eine Seitenansicht einer Gießkammer mit Gießkolben sowie Ansaugrohrzuführung zu einer Warmhalteeinrichtung.
- Die Erfindung wird anhand einer Vakuum-Druckgießmaschine beschrieben. Sie läßt sich auch für die "Evakuierung" normaler Druckgießmaschinen verwenden, wenn der Gießkolben die Einfüllöffnung verschlossen hat.
- Bezüglich dem allgemeinen Aufbau sowie den wesentlichen Funktionsmerkmalen einer Vakuum-Druckgießmaschine wird auf die eingangs erwähnte Literaturstelle und insbesondere auf die EP 0 051 310 verwiesen.
- In Fig. 1 ist von einer nur angedeuteten Druckgießmaschine 1 die feste Aufspannplatte 2 mit der hieran befestigten festen Formhälfte 3 dargestellt, die mit der beweglichen Formhälfte 4 zusammenwirkt. Zwischen der festen 3 und der beweglichen Formhälfte 4 befindet sich der Formhohlraum 5, der mit Metallschmelze zu füllen ist. Hierfür ist eine Gießkammer 6 mit einem Gießkolben 7 vorgesehen, in welche die Metallschmelze 8 über ein Saugrohr 9 aus einer Warmhalteeinrichtung 10 angesaugt wird.
- Beim Vakuum-Druckgießverfahren wird die Metallschmelze nicht durch ein Eingießverfahren, sondern durch Anlegung eines Vakuums oder Unterdrucks aus der Warmhalteeinrichtung 10 angesaugt. Dabei geschieht der Ansaugvorgang durch das Ansaugrohr 9 über die Gießkammer 6 und den Formhohlraum 5.
- Hierfür befindet sich an den Formhälften 3, 4 ein Vakuumventil 11 mit einer Vakuumanschlußleitung 12, welches zu einem Schaltventil 13 führt. Die Vakuumleitung 12 wird vom Schaltventil 13 fortgeführt zu einem Vakuumtank 14, an welchem eine Vakuumpumpe 15 zur Herstellung des Unterdrucks angeschlossen ist.
- Das Vakuumventil 11 der Gießform dient zur Absperrung der gegebenenfalls bis zu diesem Ort mittels des Gießkolbens 7 eingepreßten Metallschmelze. Ein Eindringen des Metalls in die nachfolgende Vakuumanschlußleitung 12 wird damit vermieden.
- Erfindungsgemäß wird das über das Vakuumventil 11 angelegte Vakuum über das Schaltventil 13 so in seinem Druckverlauf geregelt, daß sich der Druck im Formhohlraum 5, in der Gießkammer 6 und im Saugrohr 9 nach einer bestimmten einstellbaren Funktion pro Zeiteinheit regelt. Hierfür ist ein Rechner 16 vorgesehen, der die verschiedensten Parameter erfaßt. So wird der Unterdruck im Bereich des Vakuumventils 11 über eine zusätzliche Meßleitung 17 erfaßt und mittels einer Vakuum-Meßsonde gemessen. Diese Vakuum-Meßsonde 18 ist über ein zusätzliches Nebenschlußventil 19 an die Vakuum-Anschlußleitung 12 angeschlossen. Damit ist der Druck p in der Vakuum-Anschlußleitung 12 erfaßbar und über die Leitung 20 dem Rechner 16 zuführbar.
- Der Vakuumdruck im System kann auch über andere Meßleitungen im System dem Rechner 16 zugeführt werden. Dies ist beispielsweise durch eine Meßleitung 21 zum Vakuumtank 14 angedeutet.
- Die Regelung des Vakuums, d. h. des Unterdrucks im System erfolgt nach einem vorgegebenen Regelprogramm

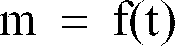
- Durch die erfindungsgemäße Möglichkeit der laufenden Meßung und Regelung des Vakuums können ganz bestimmte "Vakuumkurven" gefahren werden.
- Zunächst wird die Schmelze 8 aus der Warmhalteeinrichtung 10 über eine, am unteren Ende des Saugrohres 9 sich befindende Drossel 30 in die Gießkammer 6 durch Anlegen eines hohen Unterdrucks in der Größenordnung von p₁ ∼ 150 bis 200 mbar absolut angesaugt. Dabei bestimmt die Größe der Drossel 30, die Ansaugzeit t₁ sowie der Unterdruck p₁ die in die Gießkammer angsaugte Menge m₁ der Metallschmelze. Ein zusätzlicher Meßfühler z. B. ein Ultraschallmeßfühler 28 in der oberen Wandung der Gießkammer oder ein Widerstandsmeßfühler 28' im Angußquerschnitt der Formhälfte 4 kann die Füllstandshöhe h₁ in der Gießkammer 6 erfassen und diesen Wert über eine Meßleitung 29 dem Rechner 16 zur Auswertung zuführen.
- Der Ansaugvorgang bei Vakuumdruckgießmaschinen kann als erster Regelungsabschnitt durch Überfahren des Gießkolbens 7 über die Ansaug- oder Eintrittsöffnung 27 in die Gießkammer 6 oder durch einen entsprechend verminderten Unterdruck (Druckanstieg) beendet werden. Er entspricht dem Einfüllvorgang von Metallschmelze in eine "normale" Druckgießvorrichtung. Hierfür kann die Stellung des Gießkolbens 7 über einen Wegerfassungsgeber 31 dem Rechner 16 über eine Leitung 32 zugeführt werden, um insbesondere auch bei "normalen" Gießkammern die Kolbenstellung nach Überfahren der Einfüllöffnung 27 zu erfassen und das Vakuum zu regeln. Sensoren zur Erfassung des Weges oder der Füllstandshöhe sind an sich bekannt (s. z. B. Lit. Maschinenmarkt 1992, 40, Seite 72 - 77).
- Diesem ersten Einfüllzeitabschnitt t₁ schließt sich ein weiterer "Haltezeitabschnitt" t₂ an.
- Durch ein Halten bestimmter Unterdrücke kann das Ausgasen der Schmelze in der Gießkammer 6 und das Formevakuieren begünstigt werden. Hierfür wird über einen Zeitabschnitt t₂ nach einem kontinuierlichen Abfall des Unterdrucks (Druckanstieg) auf ein Vakuum von vorzugsweise p₂ ∼ 800 mbar absolut eine bestimmte Haltezeit des Vakuums von t₂ ∼ 0,2 bis 3 sec eingestellt. Diese Haltezeit kann sich je nach spezifischem Metallgewicht, nach der Saugrohrhöhe h₂ über oder der Füllstandshöhe h₁ in der Gießkammer und der Formkontur bemessen. Durch diesen zwischenzeitlichen Haltevorgang des Unterdruckes kann das Austreten der Gase aus der Schmelze, der Gießkammer und den Formhohlräumen gefördert und geregelt werden.
- Die Erfindung sieht weiterhin vor, daß in der ersten Ausgangsphase t₁ beim Übertritt der Schmelze 8 aus dem Saugrohr 9 in die Gießkammer 6 an der Eintrittsöffnung 27 der Gießkammer eine stetige Schmelzegeschwindigkeit v ≦ 1 m/sec aufgrund des regelbaren Unterdurcks einstellbar ist, wobei Strömungswerte vorzugsweise in der Größenordnung von unter 1 m/sec gewählt werden. Dabei wird zur Vermeidung von Turbulenzen der Gießkolben 7 in seinem unteren Bereich mit einer Umlenkfläche 26 versehen, wie dies in der Vorveröffentlichung der Anmelderin gemäß DE 41 01 592 beschrieben ist.
- Das Befüllen der Gießform geschieht in an sich bekannter Weise durch die Verschiebung des Kolbens 7 in der Gießkammer 6 in einer Vorfüll- und Formfüllphase. Während der Vorfüllphase dient die Regelung des Unterdrucks über diesen dritten Zeitabschnitt t₃ zur Absaugung der restlichen Luft- oder Gasanteile.
- Die Erfindung ist nicht auf das dargestellte und beschriebene Ausführungsbeispiel beschränkt. Sie umfaßt auch vielmehr alle fachmännischen Weiterbildungen und Ergänzungen im Rahmen des erfinderischen Grundgedankens.
Claims (13)
- Verfahren zur Regelung eines Unterdrucks bei einer Druckgieß- und insbesondere bei einer Vakuum-Druckgießmaschine zur Herstellung gas-, poren- und oxydarmer Gußstücke aus Metallen und/oder deren Legierungen, wobei mittels eines Unterdruck-Anschlußventils (12, 13) an einer Gießform (3, 4) sowie einer mit Metallschmelze (8) füllbaren Gießkammer (6), eine Unterdruckbeaufschlagung der Gießform (3, 4) sowie der Gießkammer (6) erfolgt, dadurch gekennzeichnet, daß die Unterdruckbeaufschlagung der Gießform (3, 4) bzw. der Gießkammer (6) über wenigstens ein Regelventil (13) derart erfolgt, daß der Unterdruck (p) im Formhohlraum (5) und/oder in der Gießkammer (6) nach einer regelbaren Kurve mit wengistens zwei Zeitabschnitten geregelt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, daß die Regelung des Unterdurcks nach einer progressiven, linearen oder degressiven Druck-Zeit-Funktion (

- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß die Regelung des Unterdrucks (p) als Funktion der in die Gießkammer (6) eingebrachten Menge (m) und/oder als Funktion des Gießkolbenweges (s) erfolgt.
- Verfahren nach Anspruch 1, 2 oder 3 dadurch gekennzeichnet, daß die Regelung des Unterdrucks an einer Vakuum-Druckgießmaschine mit einem Ansaugrohr (9) zur Ansaugung von Metallschmelze (8) aus einer Warmhalteeinrichtung (10) erfolgt.
- Verfahren nach Anspruch 4, dadurch gekennzeichnet, daß die Regelung des Unterdrucks (p) als Funktion der Zeit (t) und/oder der Menge (m) und/oder des Gießkolbenweges (s), derart erfolgt, daß im Saugrohr (9) und/oder in der Gießkammer (6) ein kontinuierlicher stetiger Anstieg der Schmelze (8) aus der Warmhalteeinrichtung (10) erfolgt.
- Verfahren nach einem der vorhergehenden Ansprüche 1 bis 5, dadurch gekennzeichnet, daß der Unterdruck in einer ersten Phase t₁ auf einen hohen Unterdruck p₁ ∼ 150 bis 200 mbar gehalten wird, um die Gießkammer zu füllen und daß sich eine zweite Haltephase t₂ mit einem Haltedruck p₂ ∼ 800 mbar über einen Zeitraum t₂ zur Ausgasung der Schmelze in der Gießkammer anschließt.
- Verfahren nach Anspruch 6, dadurch gekennzeichnet, daß der Halte-Unterdruck (p₂) auf einem bestimmten, vorgegebenen Wert p₂ über eine Zeitspanne t₂ derart gehalten wird, daß ein Ausgasen der Schmelze weitestgehend abgeschlossen wird.
- Verfahren nach Anspruch 6 oder 7, dadurch gekennzeichnet, daß der Halte-Unterdruck (p₂) in der Gießform (5), der Gießkammer (6) und/oder im Saugrohr (9) nach einem kontinuierlichen Abfall auf einen Unterdruck von p₂ von 200 auf 800 mbar (Anstieg des Druckes) über eine Zeitspanne t₂ ∼ 0,2 - 3 sec konstant gehalten wird, derart, daß ein Austreten der Gase aus der Schmelze erfolgt.
- Verfahren nach einem oder mehreren der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß der Unterdruck (p) mittels der Unterdruckregelung derart einstellbar ist, daß beim Übertritt der Schmelze (8) aus dem Saugrohr (9) in die Gießkammer (6) an der Eintrittsöffnung (27) der Gießkammer (6) sich eine stetige turbulenzfreie Schmelzgeschwindigkeit (v) von vorzugsweise v ≦ 1 m/sec einstellt.
- Verfahren nach einem oder mehreren der vorhergehenden Ansprüche dadurch gekennzeichnet, daß der Vakuumanschlußleitung (12) zur Erfassung des Unterdrucks eine Vakuum-Meßsonde (18) zugeordnet ist, die vorzugsweise über ein Nebenschlußventil (19) an die Vakuum-Anschlußleitung (12) angeschlossen ist.
- Verfahren nach einem oder mehreren der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß ein Rechner (16) zur Steuerung bzw. Regelung wenigstens eines Schaltventils (13) in der Vakuum-Anschlußleitung (12) vorgesehen ist.
- Verfahren nach einem oder mehreren der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß die Gießkammer (6) eine Metallschmelze-Füllstandsmeßeinrichtung (28, 28') zur Mengenerfassung aufweist, deren Meßwert zur Unterdruckregelung auswertbar ist.
- Verfahren nach einem oder mehreren der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß dem Gießkolben ein Gießkolben-Wegerfassungsgeber (31) zugeordnet ist, dessen Meßwert (s) dem Rechner (16) über eine Meßleitung (32) zuführbar ist und daß eine Regelung (

Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE4239558 | 1992-11-25 | ||
| DE4239558A DE4239558A1 (de) | 1992-11-25 | 1992-11-25 | Verfahren zur Unterdruck-Herstellung bei einer Druckgießmaschine |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0600324A1 true EP0600324A1 (de) | 1994-06-08 |
| EP0600324B1 EP0600324B1 (de) | 1999-06-16 |
Family
ID=6473581
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP93118695A Expired - Lifetime EP0600324B1 (de) | 1992-11-25 | 1993-11-20 | Verfahren zur Unterdruck-Herstellung bei einer Druckgiessmaschine |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0600324B1 (de) |
| DE (2) | DE4239558A1 (de) |
| ES (1) | ES2134820T3 (de) |
Cited By (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19628870A1 (de) * | 1996-07-17 | 1998-01-22 | Alusuisse Bayrisches Druckgus | Vorrichtung und Verfahren zur Herstellung von Druckgußteilen |
| EP1080809A1 (de) * | 1999-08-30 | 2001-03-07 | Müller Weingarten AG | Verfahren zur Regelung der Metalldosiermenge |
| DE10140657C1 (de) * | 2001-08-24 | 2002-11-07 | Mueller Weingarten Maschf | Messung des Druckes in einer Form während des Füllvorgangs |
| EP1524048A1 (de) * | 2003-10-15 | 2005-04-20 | Fondarex S.A. | Druck- oder Spritzgiessmaschine und Antriebs- bzw. Nachverdichteraggregat und Steuerung hierfür |
| US6948549B2 (en) | 2001-09-12 | 2005-09-27 | Alcan Bdw Gmbh & Co. Kg | Method for controlling a vacuum valve of a vacuum die casting device and a vacuum die casting device |
| EP1832362A1 (de) * | 2006-03-06 | 2007-09-12 | Pfeiffer Vacuum Gmbh | Vakuumdruckgussanlage und Verfahren zum Betrieb |
| JP2013022621A (ja) * | 2011-07-21 | 2013-02-04 | Honda Motor Co Ltd | 溶湯の供給方法及びその装置 |
| DE102014113570B3 (de) * | 2014-09-19 | 2015-12-24 | Ksm Castings Group Gmbh | Einrichtung zur Messung von Drücken in einem mit Schmelze füllbaren Formhohlraum einer Gießform, insbesondere einer Vakuumdruckgussform |
| CN107335789A (zh) * | 2017-08-30 | 2017-11-10 | 鞍山海望真空系统有限公司 | 双独立系统压铸高真空装置 |
| DE102016221678A1 (de) | 2016-11-04 | 2018-05-09 | Magna BDW technologies GmbH | Vorrichtung zur Herstellung von Druckgussteilen |
| DE102016221674A1 (de) | 2016-11-04 | 2018-05-09 | Magna BDW technologies GmbH | Steuerung für eine Vorrichtung zur Herstellung von Druckgussteilen |
| WO2018082939A2 (de) | 2016-11-04 | 2018-05-11 | Magna BDW technologies GmbH | Vorrichtung, steuerung und filtermodul zur herstellung von druckgussteilen, sowie verfahren dazu |
| CN110076313A (zh) * | 2019-05-05 | 2019-08-02 | 广东鸿图武汉压铸有限公司 | 一种基于真空排气和自然排气一体化的压铸模具 |
Families Citing this family (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0827794B1 (de) * | 1996-09-05 | 2001-04-18 | Electronics GmbH | Druckgiessvorrichtung und Druckgiessverfahren |
| DE19930624A1 (de) * | 1999-07-02 | 2001-01-11 | Geesthacht Gkss Forschung | Spritzgießvorrichtung |
| DE10017393B4 (de) * | 2000-04-07 | 2008-04-30 | Volkswagen Ag | Verfahren zur Herstellung von Druckgußkörpern sowie Dauerform |
| DE10022560A1 (de) * | 2000-05-10 | 2001-11-15 | Fuchs Lubritech Gmbh | Druckgießmaschine |
| DE10045594B4 (de) * | 2000-09-15 | 2006-01-19 | Hansgrohe Ag | Verfahren und Vorrichtung zum Gießen von Hohlkörpern |
| DE10054870B4 (de) * | 2000-11-06 | 2008-04-24 | Bühler Druckguss AG | Druckgiessmaschine |
| DE10357365B4 (de) * | 2002-12-11 | 2007-05-03 | Metal Technologies Sachs Giesserei Gmbh | Druckgießvorrichtung und Verfahren zum Druckgießen mit einem definierten Forminnendruck |
| DE102004057324A1 (de) * | 2004-11-27 | 2006-06-01 | Pfeiffer Vacuum Gmbh | Vakuumdruckgussverfahren |
| US8030082B2 (en) | 2006-01-13 | 2011-10-04 | Honeywell International Inc. | Liquid-particle analysis of metal materials |
| DE102007012577A1 (de) | 2007-03-13 | 2008-09-18 | Bühler Druckguss AG | Verfahren zur Entlüftung von Formen |
| ITMI20101606A1 (it) * | 2010-09-06 | 2012-03-07 | Maicopresse Spa | Dispositivo perfezionato per il riempimento di metallo fuso in camere di pressatura nelle macchine di pressofusione |
| DE102023100621A1 (de) * | 2023-01-12 | 2024-07-18 | Thomas Ninkel | Vorrichtung zum Schmelze-Dosieren an einer Druckgießmaschine |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3009218A (en) * | 1958-10-22 | 1961-11-21 | David M Morgenstern | Apparatus for vacuum feeding a die casting machine |
| US4050503A (en) * | 1973-08-16 | 1977-09-27 | Institute Po Metaloznanie I Technologia Na Metalite | Apparatus for controlling the rate of filling of casting molds |
| EP0051310A1 (de) * | 1980-11-03 | 1982-05-12 | Maschinenfabrik Müller-Weingarten AG | Druckgiessmaschine |
| DE4123463A1 (de) * | 1991-07-16 | 1993-01-21 | Audi Ag | Verfahren zur herstellung von gussstuecken mittels einer druckgiessmaschine |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CA1333497C (en) * | 1988-01-30 | 1994-12-13 | Norihiro Iwamoto | Casting control system of die cast machine |
| JPH04123860A (ja) * | 1990-09-14 | 1992-04-23 | Ryobi Ltd | 射出成形機におけるガス抜き装置制御方法と制御装置 |
-
1992
- 1992-11-25 DE DE4239558A patent/DE4239558A1/de not_active Withdrawn
-
1993
- 1993-11-20 DE DE59309656T patent/DE59309656D1/de not_active Expired - Fee Related
- 1993-11-20 EP EP93118695A patent/EP0600324B1/de not_active Expired - Lifetime
- 1993-11-20 ES ES93118695T patent/ES2134820T3/es not_active Expired - Lifetime
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3009218A (en) * | 1958-10-22 | 1961-11-21 | David M Morgenstern | Apparatus for vacuum feeding a die casting machine |
| US4050503A (en) * | 1973-08-16 | 1977-09-27 | Institute Po Metaloznanie I Technologia Na Metalite | Apparatus for controlling the rate of filling of casting molds |
| EP0051310A1 (de) * | 1980-11-03 | 1982-05-12 | Maschinenfabrik Müller-Weingarten AG | Druckgiessmaschine |
| DE4123463A1 (de) * | 1991-07-16 | 1993-01-21 | Audi Ag | Verfahren zur herstellung von gussstuecken mittels einer druckgiessmaschine |
Cited By (23)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19628870A1 (de) * | 1996-07-17 | 1998-01-22 | Alusuisse Bayrisches Druckgus | Vorrichtung und Verfahren zur Herstellung von Druckgußteilen |
| US6125911A (en) * | 1996-07-17 | 2000-10-03 | Alusuisse Bayrisches Druckguss-Werk Gmbh & Co. Kg | Method and apparatus for manufacturing die-castings |
| EP1080809A1 (de) * | 1999-08-30 | 2001-03-07 | Müller Weingarten AG | Verfahren zur Regelung der Metalldosiermenge |
| US6379609B1 (en) | 1999-08-30 | 2002-04-30 | Muller Weingarten Ag | Process for controlling the amount of metal metered |
| DE10140657C1 (de) * | 2001-08-24 | 2002-11-07 | Mueller Weingarten Maschf | Messung des Druckes in einer Form während des Füllvorgangs |
| US6948549B2 (en) | 2001-09-12 | 2005-09-27 | Alcan Bdw Gmbh & Co. Kg | Method for controlling a vacuum valve of a vacuum die casting device and a vacuum die casting device |
| EP1524048A1 (de) * | 2003-10-15 | 2005-04-20 | Fondarex S.A. | Druck- oder Spritzgiessmaschine und Antriebs- bzw. Nachverdichteraggregat und Steuerung hierfür |
| EP1832362A1 (de) * | 2006-03-06 | 2007-09-12 | Pfeiffer Vacuum Gmbh | Vakuumdruckgussanlage und Verfahren zum Betrieb |
| JP2013022621A (ja) * | 2011-07-21 | 2013-02-04 | Honda Motor Co Ltd | 溶湯の供給方法及びその装置 |
| CN105436460A (zh) * | 2014-09-19 | 2016-03-30 | Ksm铸造集团有限公司 | 铸模、特别是真空压铸模的能够由熔体填充的模具型腔中压力测量的装置 |
| CN105436460B (zh) * | 2014-09-19 | 2019-12-10 | Ksm铸造集团有限公司 | 铸模、特别是真空压铸模的能够由熔体填充的模具型腔中压力测量的装置 |
| US9427800B2 (en) | 2014-09-19 | 2016-08-30 | Ksm Castings Group Gmbh | Device for measuring pressures in a mold cavity of a casting mold that can be filled with melt, particularly a vacuum die-casting mold |
| DE102014113570B3 (de) * | 2014-09-19 | 2015-12-24 | Ksm Castings Group Gmbh | Einrichtung zur Messung von Drücken in einem mit Schmelze füllbaren Formhohlraum einer Gießform, insbesondere einer Vakuumdruckgussform |
| DE102016221674B4 (de) | 2016-11-04 | 2020-06-18 | Magna BDW technologies GmbH | Steuerung für eine Vorrichtung zur Herstellung von Druckgussteilen |
| DE102016221674A1 (de) | 2016-11-04 | 2018-05-09 | Magna BDW technologies GmbH | Steuerung für eine Vorrichtung zur Herstellung von Druckgussteilen |
| WO2018082939A2 (de) | 2016-11-04 | 2018-05-11 | Magna BDW technologies GmbH | Vorrichtung, steuerung und filtermodul zur herstellung von druckgussteilen, sowie verfahren dazu |
| DE102016221678A1 (de) | 2016-11-04 | 2018-05-09 | Magna BDW technologies GmbH | Vorrichtung zur Herstellung von Druckgussteilen |
| EP3593924A1 (de) | 2016-11-04 | 2020-01-15 | MAGNA BDW technolgies GmbH | Filtermodul in einer vorrichtung zur herstellung von druckgussteilen |
| DE102016221678B4 (de) | 2016-11-04 | 2020-07-16 | Magna BDW technologies GmbH | Vorrichtung zur Herstellung von Druckgussteilen |
| US10994329B2 (en) | 2016-11-04 | 2021-05-04 | Magna BDW technologies GmbH | Device, control system and filter module for producing die-cast parts, and method therefor |
| US10994330B2 (en) | 2016-11-04 | 2021-05-04 | Magna BDW technologies GmbH | Device, control system and filter module for producing die-cast parts, and method therefor |
| CN107335789A (zh) * | 2017-08-30 | 2017-11-10 | 鞍山海望真空系统有限公司 | 双独立系统压铸高真空装置 |
| CN110076313A (zh) * | 2019-05-05 | 2019-08-02 | 广东鸿图武汉压铸有限公司 | 一种基于真空排气和自然排气一体化的压铸模具 |
Also Published As
| Publication number | Publication date |
|---|---|
| DE4239558A1 (de) | 1994-05-26 |
| EP0600324B1 (de) | 1999-06-16 |
| DE59309656D1 (de) | 1999-07-22 |
| ES2134820T3 (es) | 1999-10-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0600324B1 (de) | Verfahren zur Unterdruck-Herstellung bei einer Druckgiessmaschine | |
| DE102004023150B4 (de) | Einspritzsystem und Gießverfahren einer Gießmaschine | |
| DE69628139T2 (de) | Verfahren zum einspritzen von flüssigmetall in einen formhohlräum | |
| DE69416715T2 (de) | Vorrichtung und Verfahren zum gesteuerten Niederdruckgiessen unter Vakuum für Aluminium oder Magnesiumlegierungen | |
| EP0051310A1 (de) | Druckgiessmaschine | |
| EP1516687B1 (de) | Verfahren zum Vakuum Druck- oder Spritzgiessen | |
| DE4313800B4 (de) | Vakuumdruckgussverfahren | |
| DE19514070C2 (de) | Steuerverfahren für eine Spritzgießvorrichtung | |
| EP1165274A1 (de) | Verfahren zum vakuum-druckgiessen und druckgiessform | |
| EP0827794B1 (de) | Druckgiessvorrichtung und Druckgiessverfahren | |
| DD202253A5 (de) | Druckgiessverfahren und -maschine | |
| WO1993001909A1 (de) | Verfahren zur herstellung von gussstücken mittels einer druckgiessmaschine | |
| DE2505648C3 (de) | Steuervorrichtung für eine Druckgießmaschine | |
| EP0483191B1 (de) | Vorrichtung und verfahren zum steuern und regeln der formfüllgeschwindigkeit und des giessdruckes einer niederdruckkokillengiessmaschine | |
| DE4419848C1 (de) | Warmkammer-Druckgießmaschine | |
| DE3206641C2 (de) | Verfahren zur Regelung der Gießgeschwindigkeit aus einem Druckofen für Metallschmelzen und Einrichtung zur Durchführung dieses Verfahrens | |
| EP0449771B2 (de) | Programmgesteuertes Einspeisen von schmelzflüssigem Metall in die Kokillen einer automatischen Stranggiessanlage | |
| DE4203337C2 (de) | Verfahren zum Stranggießen von Metallen | |
| EP0099104A2 (de) | Druckgiessverfahren | |
| DE2060681A1 (de) | Vorrichtung zur Steuerung des Druckverlaufes am Einpressteil von Giessmaschinen | |
| DE3125367A1 (de) | "verfahren zur umformung von blechteilen sowie vorrichtung zur durchfuehrung des verfahrens" | |
| CH689448A5 (de) | Verfahren und Vorrichtung zur Herstellung von Formteilen aus Metall. | |
| DE4404148A1 (de) | Verfahren und Vorrichtung zum Herstellen von Gußsträngen aus Metallen durch Stranggießen | |
| DE3240242C2 (de) | ||
| EP1057558B1 (de) | Nach einem Vakuumverfahren arbeitende Druckgiessmaschine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): CH DE ES FR GB LI |
|
| 17P | Request for examination filed |
Effective date: 19940811 |
|
| 17Q | First examination report despatched |
Effective date: 19960710 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: MUELLER WEINGARTEN AG |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE ES FR GB LI |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19990618 |
|
| REF | Corresponds to: |
Ref document number: 59309656 Country of ref document: DE Date of ref document: 19990722 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: KELLER & PARTNER PATENTANWAELTE AG |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2134820 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20051027 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20051028 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20051117 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20051118 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20051122 Year of fee payment: 13 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061130 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070601 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20061120 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20070731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061120 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20061121 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061130 Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061121 |