EP0343522A2 - Procédé et machine de reliure automatique pour exemplaires uniques - Google Patents
Procédé et machine de reliure automatique pour exemplaires uniques Download PDFInfo
- Publication number
- EP0343522A2 EP0343522A2 EP89109000A EP89109000A EP0343522A2 EP 0343522 A2 EP0343522 A2 EP 0343522A2 EP 89109000 A EP89109000 A EP 89109000A EP 89109000 A EP89109000 A EP 89109000A EP 0343522 A2 EP0343522 A2 EP 0343522A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- station
- book
- book block
- cover
- glued
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42C—BOOKBINDING
- B42C19/00—Multi-step processes for making books
Definitions
- the invention relates to a method and a system for automatic bookbinding for unique pieces and small series, the invention, however, does not relate to large-scale production.
- Type stamping, self-made, high-quality sleeves, etc. because the series production is based exclusively on newly printed paper without glue residues, creases and format fluctuations, and because the cycle times for such a series book line are so short that extensive conversions at the individual stations are not possible Purchase can be made.
- the object of the invention is to provide a method and a production line or a production system with which it is possible to bind unique pieces, single books and small series in a quality that is in no way inferior to that of artisan bookbinding, the possible variations and the To make the variety of the volumes to be bound as extensive as possible in the case of automatic production and to significantly reduce the time and cost involved in binding a single piece in comparison to conventional manual bookbinding.
- all the data required for binding the individual book is created and saved, for example, the customer and the signature are entered via data carriers, the cover type is selected, the required dimensions and colors in the form of the back-notch dimension, the dimension for the head , Foot and front cut, the thickness measurement and the cover color entered, the preparation process carried out, namely the correction of binding material and endpaper, printing out and adding the code note and storing it in a container, as well as entering the embossing including searching in the memory, selecting the font, designing the embossing, saving the embossing and storing the book.
- a specialist specifies all the bookbinding details for creating the book block, the cover and for hanging the book block in the cover, and that, based on this definition, the components required in the corresponding workstations are automatically called up in the bookbinding system, the necessary work steps are carried out on them and, if necessary, work processes which take time are cached as partially manufactured elements.
- the binding material is pushed against a contact angle at the measuring station, for example, with the help of laser light walls, the later position of the back separating notch cut, the head, foot and front cut is marked.
- the binding material By leafing through the binding material it can be checked whether the planned type area is correct and no text passages are cut off.
- the height of the stack to be bound is determined with the aid of a thickness measuring device. All dimensions are digitally coded into the computer, for example at the push of a button, and the markings are retrieved from the memory and set using an identifier. Depending on the type of cover selected, the computer determines the dimensions of the cover; these dimensions are displayed on the screen, for example.
- the desired imprint is displayed on the screen and positioned in the desired manner. For example, if there are hard covers inside the book that make processing difficult, these hard covers have to be shortened depending on the planned back separating notch cut and through a tough, supple material with the help of a suitable device tion can be extended again. Finally, a bar code is printed out in the acceptance station and coupled with the double sheets of paper enclosed with the book. The book is then placed on a mobile book shelf or book container. The data for an order, for example 100 books, are saved on a data carrier and added to the container. Instead of using such a data carrier, other types of data transmission can also be used.
- the data record assigned to the respective book block is entered into a process computer, the book address is e.g. read with a reading pen and the book block is inserted into the back notching machine and processed there.
- the section size is set and the end sheets are inserted into side receptacles.
- the first cut reduces the slope and the book block is tightened using a clamping device, e.g. Clamp, lowered and fine notched.
- the knife shape used for the back separating notching machine has trapezoidal notches, which channel channels of e.g. Notch 1.8 x 0.6 mm in the transverse direction (however, the invention is in no way limited to these dimensions of the notch channels).
- Thread-stitched book blocks are read and entered in the book block production station, but are not processed on the spine.
- the tension clamps are also links in a transport chain. After the back separation notches, the tensioning clamp is moved further with a transport chain of this type, for example hydraulically, and finally fed to the fan gluing machine, in which the open sheet edges are bent and glued. Pressure strips are integrated into the tensioning clamp system, which ensure forced contact with the glue layer. This solves a problem that was previously unsolved in fan gluing. This process is repeated several times, depending on the type of paper, and then the book block in the binding area is pressed together by pressure strips and with the tensioning clip through a drying tunnel guided. Moisture must be extracted from the glue in this drying tunnel without the polymerization process being hindered or prematurely interrupted.
- the glue must have optimal contact with the surface, which requires a dust-free back cutting notching machine. On the other hand, the glue must not run into the book block. It must also be resistant to aging, which is achieved with the aid of a water-soluble dispersion, but on the other hand must not lose too much volume because the adhesive threads in the channels can no longer fulfill their cross-binding function if the shrinkage is too great.
- the adhesive to be used must therefore meet a variety of conditions in terms of heating, moisture, airflow, air drying, feed, glue composition and energy consumption. Furthermore, it is necessary to guide the pressure strips so that the slope on the spine does not exceed a certain, permissible range.
- the book block is transferred to a cutting machine, such as a rotary gripper, in a precisely positioned position.
- a cutting machine such as a rotary gripper
- the gripper area must be small, but that the gripper should nevertheless move heavy and protruding books perfectly sideways, turn twice 90 o damped in the end position and adhere to tolerances of the order of 1/10 millimeter.
- the gripper must not build upwards because the frame of the cutting machine opposes this.
- the book block is handed over to a rich person and reaches, for example, an interim storage facility, where it is made available for hanging in the cover; however, the book block can also be hung in the cover at this point without being transferred to an interim storage facility.
- the book blocks are handed over undisturbed to the hanging street; If the book block is removed from the clipboard for further processing or for hanging in the book cover, the book block must be read in again and transferred to the hanging street in a precisely positioned position. Since freshly produced or hardened book blocks arrive from the interim storage facility, only uniform conditions can be achieved by heating to approx. 55 o to manufacture. Then the spine of the book block must be made flexible by bending and rolling over, which also exaggerates the slope and compresses it again to the required extent. The set incline is stabilized, for example, by gluing with a tape and with the help of the selected stabilizing elements.
- the inside surfaces of the cover are glued together with the back and pressed against the book block.
- the book block can remain in the bracket until the end.
- the front surfaces are glued; it is difficult to reach the joint area of the book, to release the book from the bracket in good time and still to guide it precisely.
- the preferred procedure for "pasting" presupposes that no support fabric has yet been applied to the book block spine, that the stabilizing element is already glued in the cover, that the incline is set, that the book block spine is made flexible, and that the rounding of the book block, eg with the help of compressed air.
- Pneumatic rounding is a particularly gentle and therefore preferred rounding process.
- the straight book is sealed with a glued cover with the help of press plates and sealing packages at the head and foot cut as well as with a hood around the press plates and pressed into its own book cover by compressed air.
- the degree of rounding is determined by the slope previously realized and taken into account in the cover.
- the rounded book block must harden and dry under moderate pressure. This will be done in one goods warehouse carried out.
- Another possibility of binding is that the cover is understood as a form into which the book block is pressed mechanically or with compressed air.
- the blanket making machine glues the covers or uses glued (preferably heat-sealable) covers, puts on cardboard cuts and folds in the edges.
- the raw cardboard formats are selected from a material store by the computer, trimmed on the outside by a computer-controlled cutting device (which can work on the basis of a water jet, a laser or the like) and cut into symmetrical halves. It can also be used to produce rounded corners with different profiles.
- the line web selected by the computer e.g. pulled off and held taut by a series of laterally arranged grippers which switch on one after the other.
- Glue e.g.
- the cardboard cuts and the cut back insert are positioned on the glued, stretched book linen, and the benefit is cut out (e.g. again using a water jet cutting device or the like).
- the cover covered so far is brought into the next working position, in which the wraps are programmed to be turned over and pressed or ironed on.
- the wraps are programmed to be turned over and pressed or ironed on.
- the finished whole-fabric blankets are rubbed or ironed on and placed in a buffer, which also removes moisture.
- the cover is transferred from the manufacturing station and the drying station to the embossing station.
- High demands are placed on the embossing process or the embossing press.
- a temperature control with a control range between 80 and 150 o C for example, there are about 1000 different types six fonts, each in two different sizes, six different color foils, a temperature control with a control range between 80 and 150 o C, a type and material-dependent print control, a print time control between 0.05 and 0.5 seconds, a ceiling guide in the X-axis , the Y-axis and the Z-axis and a material thickness control are required.
- the overall system makes it necessary that the embossing is largely freely programmable and that pixels can be introduced into the material in depth.
- the stabilizing element e.g. stabilization or reco sleeve according to DE-OS 35 11 646
- the stabilizing element is selected, provided with the capital band and glued into the flat cover.
- externally manufactured cover blankets e.g. publishing blankets
- the back inlays of such blankets which are often very susceptible to kinking, are also made flexible by the water-containing adhesives.
- the headband is provided in different colors and is preferably used as a heat-sealable band.
- the book that has been completed so far is stored in a repository. Following this, for example, a production control is provided, in which the book is booked out via the bar code and transferred to the transport container. The production data is delivered back to the acceptance station together with the order and from there to the customer.
- the method according to the invention or the system according to the invention can also be used for bookbinding small series, whereby Instead of the blanket production and embossing described above, simplified blanket and embossing machines (cliché embossing printing) can be used.
- the order preparation for such a small series can be designed in such a way that a sample copy with the predetermined paper is sent through a single book system, that a measurement report is then printed out, from which material blanks for the series are derived.
- lettering or cover design in black print can be carried out on white cardboard. Even externally manufactured ceilings can be stabilized with Reco sleeves and provided with a lanyard, fed to the compact road via an attachment point and processed in the manner described above.
- the customer data, the signature of the book, etc. are entered in a receiving station 1 by manual input or by Access to the memory or via data medium if the receiving station is supplied via auxiliary receiving stations that are spatially distant from the receiving station.
- the required dimensions and colors are entered in data form, namely the back notch size, head, foot and front cut, the thickness and the cover color (whereby you can choose from 24 different colors, for example).
- the preparation includes cutting the covers and the end paper, printing and folding the code slip, and storing them in the container.
- the embossing process is entered in the acceptance station, by possibly reading in the data again or visiting the memory, selecting the desired font, writing and designing the embossing and storing it.
- the binding material is retrieved from the warehouse 2 and fed to the further processing (block binding 4) via the acceptance station 1.
- block binding 4 the binding material is fed from the acceptance station 1 to a stapling station 3, from which the stapled book block is also transferred to the block binding station 4.
- the data are read into this block binding station 4 and the control or the computer is acted upon in accordance with this data.
- thread-stitching and glue-binding books the volumes to be stitched are issued for further processing, there is a rebooking, if necessary, a repeat program runs.
- the book block is input into a back separating notch device 13, in which the back of the book block is automatically trimmed, a fan-binding and gluing is performed automatically in the gluing station 14, the incline is forced, the drying performance after the gluing in the drying section 15 is monitored, the transfer of the book block to the cutting machine 5 is carried out, the cut is carried out automatically, and the book block is transferred to the suspension line 7.
- Special cases can be controlled into a special treatment station 6 from the block binding station 4.
- the cover covers are introduced into the ceiling hanging device 17.
- the book blocks arrive in an incline setting station 18, in which the calculated incline, which is ideal for the corresponding book, is set.
- the capital band and the stabilizing element are cut to length in conjunction with the ceiling production.
- the headband and the stabilizing sleeve are cut to length in station 19 and glued into the cover.
- the book block and cover are glued together, the book block is rounded in the compression station 20 and the folds are burned in in the station 21.
- the book block passes through a drying section 22, in which the applied glue is dried.
- the book block is transferred to a dry store 23.
- the book is transported through the individual stations here with the aid of a conveyor belt, a conveyor chain or the like transport device (designated by 24).
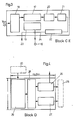
- Fig. 4 the blanket manufacturing and embossing station is shown in the block diagram.
- Cardboard and linen are introduced from a raw material store 25 into a cardboard cutting station 26 and a linen cutting station 27, in which the materials are cut. Special cases are also sorted out here.
- the cut components including the stabilizing sleeve and the headband, are transferred to the blanket production station 29, in which the gluing, placing and wrapping of the cardboard parts and the drawing in of the corners takes place.
- the blanket thus produced is then transferred to the embossing station 29, in which the blanket is embossed fully automatically in an embossing machine.
- the embossed cover blanket is stored in an intermediate blanket storage 30, e.g. on a conveyor belt, buffered.
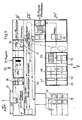
- the entire bookbinding system according to the invention is shown schematically in FIG. 5.
- 31 denotes the input of the data that takes place in the acceptance station, which can be arranged spatially separate from the system.
- the sheet stack 32 is glued in a gluing device 33 on the block spine and introduced into a fan adhesive binding device 34, in which the glued sheet stack is bound to form a book block.
- the back separating notch device 35 the back separating notch of the book block takes place.
- the (preferably hydraulic) overall drive is designated 36.
- the book block is then guided through a cutting machine 37, which performs a final trimming of the book block. At the end of station B, the book block just finished is now available.
- the book block is hung in the cover.
- Third-party ceilings are inserted into the system from outside, handled and transferred to the CE station at 40, connected to a Reco sleeve at 41 on the back and provided with a capital band at 42.
- the endless reco sleeve (e.g. in 20 widths) is automatically cut to length, as is the headband.
- the blanket thus produced is connected to the finished book block, the incline of the book block is set at 43 and the back is rounded at 44, for example with the aid of compressed air.
- the cover with the suspended book block is then temporarily stored, for example on a conveyor chain 45 with a long conveying path, and introduced into a distribution station 46, for example a shelf, where the individual finished bound volumes are prepared for shipping and packed in containers.
- the ceiling production takes place within the overall system.
- the required sizes of cardboard are automatically cut to the desired dimensions from a cardboard magazine 47 in a cardboard trimming device 48, and the stabilizing sleeves are cut to the appropriate length in a sleeve magazine, and in parallel the lines are cut from a linen magazine 49 via a glue squeegee 50 in a trimming device 51 cut to the desired size and automatically connected to the cut cardboard.
- This product then passes into the wrapping device 52 and from there into the blanket store 53, from which the finished blankets are temporarily stored and, if necessary, inserted into an embossing device 54, embossed and fed to the further processing which is carried out in the compact line CE, so that from here the further processing sequence corresponds to that of the third-party ceilings.
Landscapes
- Folding Of Thin Sheet-Like Materials, Special Discharging Devices, And Others (AREA)
- Labeling Devices (AREA)
- Automatic Assembly (AREA)
- General Factory Administration (AREA)
- Making Paper Articles (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3817463 | 1988-05-21 | ||
| DE3817463A DE3817463A1 (de) | 1988-05-21 | 1988-05-21 | Verfahren und selbsttaetig arbeitende buchbindeanlage fuer unikate und kleinserien |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0343522A2 true EP0343522A2 (fr) | 1989-11-29 |
| EP0343522A3 EP0343522A3 (fr) | 1990-07-18 |
| EP0343522B1 EP0343522B1 (fr) | 1997-03-05 |
Family
ID=6354930
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89109000A Expired - Lifetime EP0343522B1 (fr) | 1988-05-21 | 1989-05-19 | Procédé et machine de reliure automatique pour exemplaires uniques |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0343522B1 (fr) |
| AT (1) | ATE149430T1 (fr) |
| DE (2) | DE3817463A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19741755A1 (de) * | 1997-09-22 | 1999-06-24 | Kolbus Gmbh & Co Kg | Verfahren zum Einstellen einer Buchbindemaschine |
| WO2008135007A1 (fr) * | 2007-04-17 | 2008-11-13 | Peter Schmidkonz | Procédé et dispositif de réalisation commandée par logiciel de couvertures de livres destinées à des livres individuels et des tirages limités de différents formats |
| EP3118013A1 (fr) * | 2015-07-17 | 2017-01-18 | CEWE Stiftung & Co. KGaA | Systeme de fabrication de livres |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10209090A1 (de) * | 2002-03-01 | 2003-09-11 | Heidelberger Druckmasch Ag | Vorrichtung zur digitalen Werkzeugkennung für Druckend- oder Druckweiterbearbeitungsvorrichtungen |
| DE102010024232B4 (de) † | 2010-06-18 | 2024-11-07 | Kolbus Gmbh & Co. Kg | Verfahren und Vorrichtung zur Herstellung von Buchdecken |
| DE102015203006B4 (de) * | 2015-02-19 | 2020-06-18 | Bundesdruckerei Gmbh | Verfahren zur Herstellung von buchartigen Sicherheitsdokumenten mit farblich zum Sicherheitsmerkmal korrespondierendem Einband |
| DE102022120062A1 (de) * | 2022-08-09 | 2024-02-15 | Müller Martini Holding AG | Vorrichtung zur Herstellung von Druckerzeugnissen in niedrigen Auflagen |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3816866A (en) * | 1973-05-07 | 1974-06-18 | Harris Intertype Corp | Apparatus for making books |
| FR2502547B1 (fr) * | 1981-03-25 | 1985-06-14 | Ccmc | Machine automatique a relier des documents, notamment des documents comptables, sous forme de fascicules, de differentes natures et de differents formats se succedant dans un ordre quelconque |
-
1988
- 1988-05-21 DE DE3817463A patent/DE3817463A1/de not_active Withdrawn
-
1989
- 1989-05-19 DE DE58909781T patent/DE58909781D1/de not_active Expired - Fee Related
- 1989-05-19 EP EP89109000A patent/EP0343522B1/fr not_active Expired - Lifetime
- 1989-05-19 AT AT89109000T patent/ATE149430T1/de not_active IP Right Cessation
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19741755A1 (de) * | 1997-09-22 | 1999-06-24 | Kolbus Gmbh & Co Kg | Verfahren zum Einstellen einer Buchbindemaschine |
| WO2008135007A1 (fr) * | 2007-04-17 | 2008-11-13 | Peter Schmidkonz | Procédé et dispositif de réalisation commandée par logiciel de couvertures de livres destinées à des livres individuels et des tirages limités de différents formats |
| JP2010524717A (ja) * | 2007-04-17 | 2010-07-22 | シュミットコンズ,ピーター | 個別の本および異なるフォーマットサイズの表紙カバーのソフトウェア制御製造および短時間運転の方法および装置 |
| RU2450937C2 (ru) * | 2007-04-17 | 2012-05-20 | Питер ШМИДКОНЦ | Способ и устройство программно-контролируемого производства обложек для отдельных книг и малотиражных изданий различных размеров формата |
| US8313276B2 (en) | 2007-04-17 | 2012-11-20 | Peter Schmidkonz | Method and device for the software-controlled production of book covers for individual books and short runs of different format sizes |
| EP3118013A1 (fr) * | 2015-07-17 | 2017-01-18 | CEWE Stiftung & Co. KGaA | Systeme de fabrication de livres |
Also Published As
| Publication number | Publication date |
|---|---|
| DE58909781D1 (de) | 1997-04-10 |
| ATE149430T1 (de) | 1997-03-15 |
| EP0343522A3 (fr) | 1990-07-18 |
| DE3817463A1 (de) | 1989-11-30 |
| EP0343522B1 (fr) | 1997-03-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3148443A1 (de) | Schachtel mit sichtfenster sowie verfahren und vorrichtung zur herstellung einer solchen schachtel | |
| EP2508353A2 (fr) | Machine destinée à la fabrication de livres, notamment livres photo et/ou livres illustrés | |
| CH651505A5 (de) | Verfahren zum herstellen eines einbandes fuer ein buch, ein heft oder eine broschuere und vorrichtung zur durchfuehrung des verfahrens. | |
| DE4141767A1 (de) | Verfahren und anordnung zum herstellen von buechern und broschueren | |
| DE3215298A1 (de) | Gebundenes buch sowie verfahren zu seiner herstellung | |
| EP2190675A1 (fr) | Procédé et dispositif de réalisation commandée par logiciel de couvertures de livres destinées à des livres individuels et des tirages limités de différents formats | |
| DE102016218047B4 (de) | Verfahren, Vorrichtung und System zur Herstellung eines buchförmigen Ausweis-, Wert- oder Sicherheitsdokument und buchförmiges Ausweis-, Wert- oder Sicherheitsdokument | |
| DE3913604A1 (de) | Verfahren und vorrichtung zum aufbringen von unterschriftsstreifen auf ausweiskarten | |
| DE19922100A1 (de) | Verfahren und Einrichtung zum Fächerklebebinden von Büchern, Buchblöcken, Broschüren und dgl. | |
| DE69000715T2 (de) | Vorrichtung zum automatischen anbringen von etiketten auf kartons und paletten. | |
| EP0343522B1 (fr) | Procédé et machine de reliure automatique pour exemplaires uniques | |
| EP3515721B1 (fr) | Dispositif et procédé de séparation et de tri de pages doubles pour document d'identité, de valeur ou de sécurité en forme de livre, procédé et système de fabrication d'un document d'identité, de valeur ou de sécurité en forme de livre | |
| DE69223812T2 (de) | Vorrichtung und verfahren zum herstellen von akten | |
| DE2242576C2 (de) | Verfahren und Vorrichtung zum Falten mehrerer übereinanderliegender, klammergehefteter Papierbogen | |
| EP1834804B1 (fr) | Procédé et dispositif destinés à l'installation d'une enveloppe | |
| EP1425186A1 (fr) | Procede et dispositif pour relier automatiquement mecaniquement des corps d'ouvrage dans un cycle de travail | |
| DE60317844T2 (de) | Gerät zur automatischen Bindung von Heften mit variabeler Dicke mit zumindestens zwei Zufuhrvorrichtungen | |
| CH691050A5 (de) | Verfahren für das Herstellen von Büchern, Magazinen oder Broschüren. | |
| DE19959935A1 (de) | Verfahren und Vorrichtung zum Begazen und Hinterkleben von Buchrücken insbesondere für Kleinauflagen | |
| DE102018103625A1 (de) | System zur herstellung und bearbeitung eines buchförmigen ausweis-, wert- oder sicherheitsdokuments und herstellverfahren | |
| DE3723814C2 (fr) | ||
| DE102016218045B4 (de) | Verfahren und Vorrichtung zur Herstellung eines Passbuchblocks für ein buchartigen Ausweis-, Wert- oder Sicherheitsdokument, System zur Herstellung eines buchartigen Ausweis-, Wert- oder Sicherheitsdokument und buchartiges Ausweis-, Wert- oder Sicherheitsdokument | |
| DE10118133B4 (de) | Verfahren zum Prägen und Falzen von Blattgut und Universalfalzvorrichtung | |
| DE60121090T2 (de) | Verfahren zur Herstellung von Gruppen von gedruckten Seiten, zum Vorbereiten von Büchern, und damit hergestellten Gruppen von gedruckten Seiten | |
| DE102016218044B4 (de) | Zusammenstellvorrichtung und ein Verfahren zum Vereinzeln und Sortieren von Doppelseiten für ein buchförmiges Ausweis-, Wert- oder Sicherheitsdokuments, Verfahren und System zur Herstellung eines buchförmiges Ausweis-, Wert- oder Sicherheitsdokuments |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH DE ES FR GB GR IT LI LU NL SE |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AT BE CH DE ES FR GB IT LI NL SE |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH DE ES FR GB IT LI NL SE |
|
| 17P | Request for examination filed |
Effective date: 19901103 |
|
| 17Q | First examination report despatched |
Effective date: 19920709 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE ES FR GB IT LI NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRE;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED.SCRIBED TIME-LIMIT Effective date: 19970305 Ref country code: ES Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19970305 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19970305 |
|
| REF | Corresponds to: |
Ref document number: 149430 Country of ref document: AT Date of ref document: 19970315 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 58909781 Country of ref document: DE Date of ref document: 19970410 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19970605 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19970610 |
|
| EN | Fr: translation not filed | ||
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: FC Ref country code: FR Ref legal event code: RN |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20010503 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20010518 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20010521 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20010607 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20010627 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20010721 Year of fee payment: 13 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020519 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020519 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020531 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020531 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021203 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20020519 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030131 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |