Background technology
Traditional storage battery sheet operation is generally finished by full craft or semi-hand, so not only time-consuming but also the effort, production efficiency is low, cost is high, workman's labour intensity is large, and owing to contain heavy metal lead on the pole plate, the workman directly contacts lead powder dirt, and is larger to health hazards, along with the market demand is increasing, the environmental demands of storage battery production link is more and more higher, and the automation of storage battery sheet operation seems and is even more important.
Positive and negative pole plate automatic conveying device is mainly used in orderly the moving to of the positive and negative pole plate in positive plate stocker storehouse and the minus plate stocker storehouse cooperated on the bag sheet platform and wraps the sheet operation, traditional modes such as flaker employing manipulator grasp Mobile pole plate, not only need a plurality of grasping movement to work in coordination, efficient is lower, and manipulator can cause damage to pole plate, destroy easily the active substance on it, cause getting rid of powder, mashed sheet, thereby reduce accumulator quality and capacity, adopt the pneumatic manipulator of controlling, noise also can be larger, and the maintenance and repair cost is higher; Traditional manipulator is carried pole plate in addition, in order to save equipment cost, usually adopt the mobile positive and negative pole plate of same manipulator crawl, bump positive plate and removed again to bump minus plate, cause the mutual pollution between the positive and negative pole plate, can affect accumulator quality and capacity equally.
The utility model content
For the positive and negative pole plate automatic conveying device that overcomes prior art damages pole plate easily, destroy the active substance on the pole plate, cause the cross pollution between the positive and negative pole plate, affect the deficiency of accumulator quality and capacity, the utility model provides a kind of can not damage pole plate, the positive and negative pole plate automatic conveying device that positive and negative pole plate can cross pollution.
The technical scheme that its technical matters that solves the utility model adopts is:
A kind of positive and negative pole plate automatic conveying device of flaker, be included in the erecting frame that the lower transverse reciprocating of PLC control moves, and be installed in pole plate mobile device on the erecting frame, described pole plate mobile device comprises the cylinder that is fixed on the erecting frame, and driven the vacuum cup vertically move by cylinder, two of described pole plate mobile devices are one group, and corresponding absorption, mobile positive plate and minus plate are provided with one group of above pole plate mobile device on the described erecting frame respectively.
As improvement of the technical scheme, described vacuum cup is installed in by cylinder and drives on the connection bracket vertically move, and described connection bracket comprises the piston rod that is connected with cylinder and the shock strut of built-in stage clip.
As further improvement in the technical proposal, described erecting frame is installed on the sliding rail of horizontally set, also is provided with under PLC control and drives the motor that erecting frame moves back and forth along sliding rail.
As the another kind of embodiment of technique scheme, described erecting frame is installed on the sliding rail of horizontally set, also is provided with under PLC control and drives the fixedly cylinder that erecting frame moves back and forth along sliding rail.
The beneficial effects of the utility model are: adopt vacuum cup to replace traditional moving structures such as manipulator, high efficiency can not damaged the damage pole plate, has guaranteed quality and the capacity of storage battery; Two of pole plate mobile devices are one group, carry respectively positive plate and minus plate, have avoided the cross pollution between the positive and negative pole plate; Simple and reasonable, noise is low, and the maintenance and repair cost is lower, and is conducive to many group combination installations, and synchronous working forms manufacturing line, and degree of automation and production efficiency improve greatly.
The specific embodiment
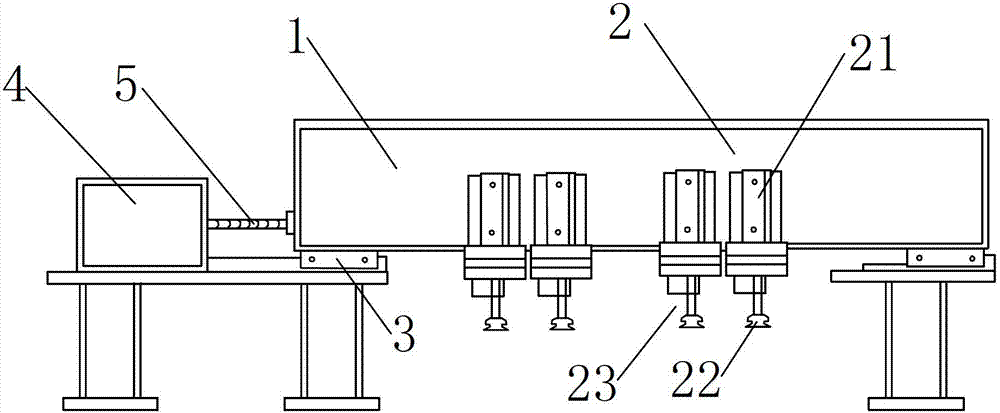
See figures.1.and.2, the positive and negative pole plate automatic conveying device of a kind of flaker of the present utility model, be included in the erecting frame 1 that the lower transverse reciprocating of PLC control moves, and be installed in pole plate mobile device 2 on the erecting frame 1, described pole plate mobile device 2 comprises the cylinder 21 that is fixed on the erecting frame 1, and driven the vacuum cup 22 that vertically moves by cylinder 21,2 two of described pole plate mobile devices are one group, corresponding absorption, mobile positive plate and minus plate are provided with one group of above pole plate mobile device 2 on the described erecting frame 1 respectively.
Traditional flaker adopts manipulator crawl Mobile pole plate, not only need a plurality of grasping movement to work in coordination, efficient is lower, and traditional moving structures such as manipulator can cause damage to pole plate, destroys easily the active substance on it, cause getting rid of powder, mashed sheet, thereby reduce accumulator quality and capacity, this product adopts vacuum cup 22 absorption pole plates, thereby has avoided the damage pole plate, ensured quality and the capacity of storage battery, structure is more simple and reliable simultaneously.In order to prevent the cross pollution between positive plate and the minus plate, 2 two of pole plate mobile devices are one group, adsorb respectively positive plate and minus plate.
Adopt the transverse shifting of PLC control erecting frame 1, be provided with one group of above pole plate mobile device 2 on the erecting frame 1, rationally distributed, expansion is good, the action of carrying many group pole plates is finished in synchronized operation, can many group flaker structures be set correspondence, cooperates synchronously and finishes many group bag sheet operations, degree of automation and production efficiency improve greatly, reduced cost, made production law orderly, steady quality is reliable, be easy to installation and maintenance, the classification that is conducive to the waste material waste residue is recycled.
As improvement of the technical scheme, described vacuum cup 22 is installed in by cylinder 21 and drives on the connection bracket 23 that vertically moves, and described connection bracket 23 comprises the piston rod 231 that is connected with cylinder 21 and the shock strut 232 of built-in stage clip.Cylinder 21 is by piston rod 231 transmissions, driving vacuum cup 22 vertically moves, be provided with shock strut 232, being conducive to vacuum cup 22 cooperates when adsorbing pole plate, the stage clip compression of shock strut 232 the insides, vacuum cup 22 is applied certain pressure, make the absorption pole plate more reliable, bag sheet platform owing to flaker can carry out lifting along with the quantity difference of pole plate stack in addition, quantity of polar plate in the pole plate stocker storehouse also can increase and decrease, so the fore-and-aft distance of vacuum cup 22 from the vertex to the positive/negative plate is all different, being provided with shock strut 232 can make piston rod 231 dropping distances fix, remaining distance is remedied by shock strut 232 compressions, prevents from damaging pole plate, and equipment is impacted.
Further, described erecting frame 1 is installed on the sliding rail 3 of horizontally set, also is provided with under PLC control and drives the motor 4 that erecting frame 1 moves back and forth along sliding rail 3.In this specific embodiment, motor 4 is servomotor, mouth is connected with screw rod 5, the other end of screw rod 5 links to each other with erecting frame 1, it is mobile at sliding rail 3 that the rotation of motor 4 drives erecting frame 1 by screw rod 5, the moving direction of the forward counter-rotating control erecting frame 1 of motor 4, operation is more steadily reliable, and low noise, easy care, long service life is owing to the distance that moves back and forth of erecting frame 1 is roughly fixed, in order to save equipment cost, sliding rail 3 is arranged on erecting frame 1 two ends, erecting frame 1 centre portion is unsettled, has reduced the length of sliding rail 3, has reduced equipment cost.
This product is arranged on casket body and positive plate stocker storehouse and the top, minus plate stocker storehouse of flaker, positive plate stocker storehouse and minus plate stocker storehouse are separately positioned on casket body both sides, same transverse horizontal is put, along with erecting frame 1 transverse reciprocating moves, two minus plates that are one group pole plate mobile device 2 can successively adsorb respectively the positive plate in positive plate stocker storehouse and minus plate stocker storehouse move on the bag sheet platform in the casket body, thereby assisting to finish wraps sheet and move.
During work, erecting frame 1 moves along sliding rail 3 under the motor 4 of PLC control drives, when erecting frame 1 is shifted to minus plate stocker storehouse this side, cylinder 21 actions of corresponding pole plate mobile device 2, driving vacuum cup 22 by piston rod 231 moves down, vacuum cup 22 touches minus plate primary piston bar 231 to be continued to move down, so that the compression of the stage clip in the shock strut 232 buffering, vacuum cup 22 adsorbs the minus plate that is arranged in minus plate stocker storehouse, under cylinder 21 and piston rod 231 drives, move, erecting frame 1 is laterally mobile under motor 4 drives, vacuum cup 22 is moved down into the minus plate of absorption on the bag sheet platform at casket body place and decontrols, move on the vacuum cup 22 and reset, baffle plate conveying device transports the dividing plate pad on minus plate, erecting frame 1 moves to top, positive plate stocker storehouse again, another pole plate mobile device 2 of same group drives vacuum cup 22 and moves down the absorption positive plate, then move on, erecting frame 1 moves back to casket body top, pole plate mobile device 2 moves down the positive plate of absorption on the dividing plate that is placed into bag sheet platform, automatically cut baffle plate device and cut off dividing plate, the folding bag sheet devices promotes the dividing plate folding bag on positive plate, bag sheet platform descends, erecting frame 1 and pole plate mobile device 2 again cooperating move to minus plate and positive plate on the utmost point group who folds by vacuum cup 22, repeatedly, reach after the required quantity of polar plate, bag sheet platform drops to casket body bottom, and the utmost point group that pusher is good with the folding bag sheet shifts onto on the utmost point group load-transfer device.
In order to raise the efficiency, save work-hours, two pole plate mobile devices 2 of same group also can adopt the mode of working simultaneously, when one of them pole plate mobile device 2 adsorbs the positive plate that promotes in the positive plate stocker storehouses by vacuum cup 22, the vacuum cup 22 of another pole plate mobile device 2 is placed into the minus plate of absorption on the bag sheet platform, and reset, then erecting frame 1 moves along sliding rail 3 under the motor 4 of PLC control drives, the positive plate that pole plate mobile device 2 adsorbs vacuum cup 22 is placed on the bag sheet platform and has filled up on the minus plate of dividing plate, another pole plate mobile device 2 is by the minus plate in the vacuum cup 22 absorption lifting minus plate stocker storehouses, then the erecting frame transverse shifting so repeats just reaching conveying, minus plate cooperates the purpose of bag sheet.
As another kind of embodiment, described erecting frame 1 is installed on the sliding rail 3 of horizontally set, also be provided with under PLC control and drive the fixedly cylinder that erecting frame 1 moves back and forth along sliding rail 3, fixedly the cylinder speed of response is faster, and equipment cost is lower than servomotor, shortcoming be vibrate larger, not steady, noise is arranged, safeguard relative complex, service life is shorter.
Certainly, the utility model can also have other structural distortion except above-mentioned embodiment, and for example: erecting frame 1 adopts the mode that hangs to fix, and has replaced sliding rail 3 parts; Vacuum cup 22 is directly installed on the spring end that is connected with piston rod 231, has replaced shock strut 232 parts; Motor 4 adopts stepping motor as engine installation, and these equivalent technical solutions also should be within its protection domain.