WO2024143239A1 - 偏光膜製造用ポリビニルアルコール系フィルムおよびその製造方法、並びにそれを用いてなる偏光膜 - Google Patents
偏光膜製造用ポリビニルアルコール系フィルムおよびその製造方法、並びにそれを用いてなる偏光膜 Download PDFInfo
- Publication number
- WO2024143239A1 WO2024143239A1 PCT/JP2023/046305 JP2023046305W WO2024143239A1 WO 2024143239 A1 WO2024143239 A1 WO 2024143239A1 JP 2023046305 W JP2023046305 W JP 2023046305W WO 2024143239 A1 WO2024143239 A1 WO 2024143239A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- polyvinyl alcohol
- film
- polarizing film
- polarizing
- solution
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B5/00—Optical elements other than lenses
- G02B5/30—Polarising elements
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C41/00—Shaping by coating a mould, core or other substrate, i.e. by depositing material and stripping-off the shaped article; Apparatus therefor
- B29C41/24—Shaping by coating a mould, core or other substrate, i.e. by depositing material and stripping-off the shaped article; Apparatus therefor for making articles of indefinite length
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J5/00—Manufacture of articles or shaped materials containing macromolecular substances
- C08J5/18—Manufacture of films or sheets
-
- H—ELECTRICITY
- H10—SEMICONDUCTOR DEVICES; ELECTRIC SOLID-STATE DEVICES NOT OTHERWISE PROVIDED FOR
- H10K—ORGANIC ELECTRIC SOLID-STATE DEVICES
- H10K50/00—Organic light-emitting devices
- H10K50/80—Constructional details
- H10K50/86—Arrangements for improving contrast, e.g. preventing reflection of ambient light
-
- H—ELECTRICITY
- H10—SEMICONDUCTOR DEVICES; ELECTRIC SOLID-STATE DEVICES NOT OTHERWISE PROVIDED FOR
- H10K—ORGANIC ELECTRIC SOLID-STATE DEVICES
- H10K59/00—Integrated devices, or assemblies of multiple devices, comprising at least one organic light-emitting element covered by group H10K50/00
- H10K59/10—OLED displays
Definitions
- the present invention relates to a polyvinyl alcohol-based film for use in the manufacture of polarizing films, and more specifically, to a polyvinyl alcohol-based film for use in the manufacture of polarizing films that has low levels of impurities eluted into the aqueous boric acid solution used in the crosslinking and stretching process and other steps during the manufacture of polarizing films, thereby preventing contamination of chemical tanks during the manufacture of polarizing plates and enabling the manufacture of polarizing films with good productivity.
- liquid crystal display devices have made remarkable progress and are now widely used in smartphones, tablets, personal computers, liquid crystal televisions, projectors, in-vehicle panels, and the like.
- a polarizing film is used in such liquid crystal display devices, and the polarizing film is mainly a polyvinyl alcohol film with iodine adsorbed and aligned.
- the polarizing film is mainly a polyvinyl alcohol film with iodine adsorbed and aligned.
- polarizing films that are far superior in polarization performance to conventional products, have no color unevenness, and are wide and long.
- impurities include low-molecular-weight polyvinyl alcohol-based resins (including oligomers) present in the polyvinyl alcohol-based film.
- low-molecular-weight polyvinyl alcohol resins eluted in chemicals containing boric acid form associations with iodine and boric acid in the chemicals to become foreign matter (precipitates) containing polyvinyl alcohol resins. If these foreign matter float in the chemicals and adhere to the surface of the polarizing film during processing, they will cause foreign matter defects in the final polarizing film, and therefore must be removed.
- the polyvinyl alcohol film which is the raw material, is generally produced by dissolving the polyvinyl alcohol resin as a raw material in water and using a continuous casting method from this aqueous solution (film-forming solution). Specifically, the aqueous solution of the polyvinyl alcohol resin is discharged and cast onto a casting mold such as a cast drum or endless belt to produce a film, and the resulting film is peeled off from the casting mold and transported in the length direction (MD direction) while being dried and heat-treated.
- a casting mold such as a cast drum or endless belt
- Methods proposed to improve the above problems include, for example, a polyvinyl alcohol film that reduces the amount of polyvinyl alcohol resin eluted into water (see Patent Document 1) and a method for removing foreign matter (precipitates) containing polyvinyl alcohol resin that occurs in a chemical tank (see Patent Document 2).
- Patent Document 2 enables long-term continuous operation by using a bubbling device to efficiently remove foreign matter (precipitates) containing polyvinyl alcohol-based resin generated in the chemical tank, thereby improving production efficiency.
- a bubbling device to efficiently remove foreign matter (precipitates) containing polyvinyl alcohol-based resin generated in the chemical tank, thereby improving production efficiency.
- the present inventors have focused on the relationship between the differential molecular weight distribution curve in gel permeation chromatography and the amount of polyvinyl alcohol resin eluted from a polyvinyl alcohol film in a boric acid solution, and have found that when the half-width of the peak corresponding to polyvinyl alcohol in the differential molecular weight distribution curve in gel permeation chromatography is within a specific range, the above problem can be solved, chemical contamination in the polarizing film manufacturing process can be suppressed, and polarizing films with few foreign matter defects can be manufactured with good productivity.
- the half-width of the peak corresponding to polyvinyl alcohol in the differential molecular weight distribution curve of gel permeation chromatography of the polyvinyl alcohol film must be 0.9 or less, preferably 0.8 or less, and particularly preferably 0.75 or less.
- the lower limit of the half width is usually 0.3 or more, and preferably 0.5 or more.
- the differential molecular weight distribution curve in the present invention is a differential molecular weight distribution curve obtained by gel permeation chromatography measurement using polyethylene oxide and polyethylene glycol as standard samples, in which the horizontal axis represents the common logarithm log M of the molecular weight M and the vertical axis represents dw/dlogM obtained by differentiating the concentration fraction w by the common logarithm log M of the molecular weight M.
- the half width indicates the width of logM (full width at half maximum) which is half the maximum value of dw/dlogM in the differential molecular weight distribution curve.
- the molecular weight M here is the molecular weight calculated based on a standard sample.
- the film may be dissolved in a mobile phase or the like and then measured as it is, or components other than the polyvinyl alcohol-based resin may be removed in advance as a pretreatment by an operation such as extraction, and then the measurement may be performed.
- the elution amount in the elution test in a boric acid solution carried out under the following condition (A) is equal to or less than the above upper limit, the elution amount of the polyvinyl alcohol-based resin into a chemical solution containing boric acid during the production of the polarizing film is small, and contamination of the chemical solution during the production of the polarizing film can be suppressed, resulting in a polyvinyl alcohol-based film with few foreign matter defects and excellent productivity.
- Methods for controlling the half-width of the peak corresponding to polyvinyl alcohol in the differential molecular weight distribution curve of the gel permeation chromatography of the polyvinyl alcohol-based film to a predetermined range include, for example, a method of using the difference in solubility between low and high molecular weight components to wash the polyvinyl alcohol-based resin with a solvent to remove the low molecular weight components, and a method of reducing the variation in molecular weight of the polyvinyl alcohol-based resin obtained by controlled radical polymerization.
- a method using controlled radical polymerization is preferred, and in particular, a method using an organic cobalt complex as a control agent is preferred in terms of ease of control of the half-width.
- the method for producing the polyvinyl alcohol-based film will be described in more detail below in the order of steps, but the polyvinyl alcohol-based film is not limited to these embodiments.
- the present polyvinyl alcohol film is preferably produced through the following steps (A) to (C), and preferably also through step (D) as necessary.
- the diameter of such a casting drum is preferably from 2 to 5 m, particularly preferably from 2.4 to 4.5 m, and further preferably from 2.8 to 4 m. If the diameter is too small, the drying zone on the cast drum becomes short, making it difficult to increase the speed, whereas if the diameter is too large, transportability tends to decrease.
- the upper limit of the drying time when drying with a heated roll is preferably 60 seconds or less, particularly preferably 55 seconds or less, further preferably 50 seconds or less, and particularly preferably 45 seconds or less, and the lower limit is preferably 20 seconds or more, particularly preferably 25 seconds or more, further preferably 27 seconds or more, and particularly preferably 30 seconds or more. If the hot roll drying time is too long, the dyeability during the production of the polarizing film tends to decrease, and if it is too fast, the film becomes more susceptible to wrinkling or folding during the swelling step during the production of the polarizing film, tending to deteriorate the appearance of the polarizing film.
- Step (D) is a step of heat treating the obtained film (heat treatment step).
- the film that has been subjected to the above step (C) may be subjected to a heat treatment, for example, in a drying oven, a floating dryer or the like.
- the temperature of the heat treatment means, for example, the temperature in a drying oven when the heat treatment is performed in a drying oven, and the temperature in a floating dryer when the heat treatment is performed in a floating dryer.
- the upper limit of the heat treatment temperature is preferably 140° C. or less, particularly preferably 135° C. or less, further preferably 130° C. or less, and particularly preferably 125° C. or less.
- the lower limit is preferably 60° C. or more, particularly preferably 75° C.
- the weight swelling degree of the present polyvinyl alcohol film is preferably 185 to 200%.
- the lower limit is particularly preferably 186% or more, and more preferably 187% or more.
- the upper limit is particularly preferably 199% or less, and more preferably 198% or less. If the weight swelling degree is lower than the above range, the stretchability during the preparation of the polarizing film tends to decrease, whereas if it exceeds the above range, the stretchability improves but the polarizing performance of the polarizing film tends to decrease.
- the elastic modulus of the polyvinyl alcohol film is preferably 250 N/mm2 or more , particularly preferably 290 N/ mm2 or more, and more preferably 400 N/ mm2 or more.
- the upper limit is preferably 800 N/ mm2 or less, particularly preferably 700 N/ mm2 or less, and more preferably 600 N/ mm2 or less. If the elastic modulus is too low, breakage tends to occur easily during production of a thin polarizing film, whereas if it is too high, the stretchability of the polarizing film during production tends to decrease.
- the amount of polyvinyl alcohol resin dissolved in water (ppm/ m2 ) in the polyvinyl alcohol film is preferably 900 ppm/ m2 or less, particularly preferably 800 ppm/ m2 or less, further preferably 700 ppm/ m2 or less, and particularly preferably 650 ppm/ m2 or less.
- the lower limit is usually 0 ppm/ m2 or more, preferably 50 ppm/ m2 or more, and particularly preferably 100 ppm/ m2 or more.
- the polyvinyl alcohol-based film obtained by the manufacturing method according to one embodiment of the present invention is useful for optical applications. In particular, it is extremely useful as a raw film for a polarizing film.
- a polarizing film and a polarizing plate made of the polyvinyl alcohol-based film.
- the swelling process is carried out before the dyeing process, for example, by immersing the film in a swelling liquid (swelling bath).
- the swelling process not only cleans dirt from the surface of the polyvinyl alcohol-based film, but also has the effect of preventing uneven dyeing by swelling the polyvinyl alcohol-based film.
- water is usually used as the swelling liquid.
- the main component of the swelling liquid is water, it may contain additives such as iodide compounds and surfactants, alcohol, etc.
- the temperature of the swelling bath is usually around 10 to 45°C, and the immersion time in the swelling bath is usually around 0.1 to 10 minutes.
- the dyeing process is carried out by contacting the film with a liquid (dyeing solution) containing iodine or a dichroic dye, for example by immersing the film in the dyeing solution.
- the dyeing solution is usually an aqueous solution of iodine-potassium iodide, with an appropriate iodine concentration of 0.1-2 g/L and a potassium iodide concentration of 1-100 g/L.
- the dyeing solution may contain a small amount of an organic solvent that is compatible with water in addition to the water solvent. A dyeing time of about 30-500 seconds is practical.
- the dyeing temperature is preferably 5-50°C.
- the boric acid crosslinking process is carried out using boron compounds such as boric acid and borax.
- the boron compound is used in the form of an aqueous solution or an aqueous-organic solvent mixture at a concentration of about 10 to 100 g/L, and it is preferable to have potassium iodide coexist in the liquid in terms of stabilizing the polarization performance.
- the processing temperature is preferably about 30 to 70°C, and the processing time is preferably about 0.1 to 20 minutes, and a stretching operation may be performed during processing as necessary.
- the film is preferably stretched 3 to 10 times in one axial direction, and particularly preferably 3.5 to 7 times.
- slight stretching may also be performed in the direction perpendicular to the stretching direction.
- the temperature during stretching is preferably 40 to 170°C.
- the final stretching ratio need only be set within the above range, and the stretching operation may be performed not only in one step, but multiple times in the manufacturing process.
- the drying process is carried out, for example, using a dryer at 40 to 100°C for 0.1 to 10 minutes.
- the single transmittance of the polarizing film of this embodiment is preferably 43% or more. If the single transmittance is too low, it tends not to be possible to achieve high brightness in liquid crystal displays.
- the single transmittance is a value obtained by measuring the light transmittance of the polarizing film alone using a spectrophotometer.
- the polarizing film of this embodiment is suitable for producing a polarizing plate having little color unevenness and excellent polarizing performance.
- the polarizing plate is produced by laminating an optically isotropic resin film as a protective film on one or both sides of the polarizing film of the present embodiment via an adhesive.
- the protective film include a film made of an acetyl cellulose-based resin such as triacetyl cellulose or diacetyl cellulose, a film made of a polyester-based resin such as polyethylene terephthalate, polyethylene naphthalate, or polybutylene terephthalate, a polycarbonate-based resin film, a cycloolefin-based resin film, an acrylic-based resin film, and a film made of a chain olefin-based resin such as a polypropylene-based resin.
- the lamination method is a known method, for example, by uniformly applying a liquid adhesive composition to the polarizing film, the protective film, or both, and then laminating and pressing the two together, followed by heating or irradiating with active energy rays.
- the polarizing films and polarizing plates obtained using the polyvinyl alcohol-based film for manufacturing polarizing films of this embodiment have excellent polarization performance, and are preferably used in liquid crystal display devices such as portable information terminals, personal computers, televisions, projectors, signage, electronic desk calculators, electronic clocks, word processors, electronic paper, game consoles, videos, cameras, photo albums, thermometers, audio equipment, instruments for automobiles and machinery, sunglasses, anti-glare glasses, stereoscopic glasses, wearable displays, foldable displays, anti-reflection layers for display elements (CRT, LCD, organic EL, electronic paper, etc.), optical communication devices, medical devices, building materials, toys, etc.
- liquid crystal display devices such as portable information terminals, personal computers, televisions, projectors, signage, electronic desk calculators, electronic clocks, word processors, electronic paper, game consoles, videos, cameras, photo albums, thermometers, audio equipment, instruments for automobiles and machinery, sunglasses, anti-glare glasses, stereoscopic glasses, wearable displays, foldable
- ⁇ Weight swelling degree> A polyvinyl alcohol film was cut into a size of 100 mm x 100 mm and immersed in an ion exchange water tank adjusted to 30 ° C for 15 minutes. After immersion, the film was taken out, spread on a filter paper (5A), and the filter paper (5A) was further placed on the film, and a SUS plate of 150 mm x 150 mm x 4 mm (4.4 g / cm 2 ) was placed on top of the filter paper (5A) for 5 seconds to remove water adhering to the film surface. The film was quickly placed in a weighing bottle, and its weight was measured, which was taken as the film weight A when swollen. The above operation was performed in an environment of 23 ° C and 50% RH.
- the film was stretched to a total stretch ratio of 3 times while being immersed in an aqueous solution at 30°C containing 0.5 g/L of iodine and 2.5 g/L of potassium iodide for 20 seconds, and the polyvinyl alcohol-based film was cut at the chuck section to obtain a dyed polyvinyl alcohol-based film.
- the dyed polyvinyl alcohol-based film was immersed in 100 mL of an aqueous solution at 60°C containing 44 g/L of boric acid and 120 g/L of potassium iodide for 5 minutes to obtain an eluate.
- a color reagent a reagent consisting of 500 g of ion-exchanged water, 7.4 g of potassium iodide, 0.65 g of iodine, and 10.6 g of boric acid
- the absorbance at a wavelength of 690 nm was measured using a spectrophotometer (Shimadzu UV-3600Plus) and a quartz cell with an optical path length of 100 mm, and a calibration curve was created by plotting the polyvinyl alcohol resin concentration (ppm) against the absorbance at 690 nm.
- ⁇ Elastic modulus> A test piece measuring 120 mm in length and 15 mm in width was cut out from the obtained polyvinyl alcohol film and conditioned in a thermo-hygrostat at 23°C and 40% RH for at least 24 hours. Then, a tensile test was carried out in the longitudinal direction in an environment of 23°C and 40% RH using a Shimadzu Corporation "Precision Universal Testing Machine, Autograph (AG-IS)" in accordance with JIS K7127:1999 (tensile speed 1000 mm/min, chuck distance 50 mm) to obtain the elastic modulus (N/ mm2 ).
- AG-IS Precision Universal Testing Machine, Autograph
- II cobalt
- the thus obtained methanol solution of polyvinyl acetate was diluted with methanol to a concentration of 3.5% by mass, and charged into the same reactor as above.
- the reactor was immersed in a water bath and heated to an internal temperature of 50° C. 120 parts by mass of a 3.6% by mass solution of sodium hydroxide in methanol was added thereto to start the saponification reaction. As the saponification reaction proceeds, the saponified product precipitates, but stirring was continued as it is. Two hours after the addition of the methanol solution of sodium hydroxide, the obtained saponified product was filtered out and charged into the reactor again, to which 500 parts by mass of methanol was added and heated to 50° C.
- Example 2 After the polyvinyl alcohol-based film that had been subjected to the drying process was peeled off from the base film, a polyvinyl alcohol-based film was obtained in the same manner as in Example 1, except that the heat treatment temperature in the drying furnace was changed to 130° C. The properties of the obtained polyvinyl alcohol-based film are shown in Table 1.
- composition was prepared by blending 12 parts by mass of glycerin as a plasticizer and 0.1 parts by mass of polyoxylaurylamine as a surfactant with 100 parts by mass of the polyvinyl alcohol-based resin (2) obtained in the above Synthesis Example, and ion-exchanged water was added to the composition so that the concentration of the composition became 19% by mass. The composition was then heated and dissolved at 130° C. for 1 hour using an autoclave to obtain an aqueous polyvinyl alcohol-based resin solution.
- This aqueous polyvinyl alcohol resin solution was cast onto a polyethylene terephthalate (PET) film (125 ⁇ m) as a base film so that the film thickness after drying would be 45 ⁇ m, and then dried for 7 minutes in a drying oven heated to 110° C. Thereafter, the polyvinyl alcohol film that had been subjected to the drying process was peeled off from the base film to obtain a polyvinyl alcohol film.
- PET polyethylene terephthalate
- Comparative Example 2 A polyvinyl alcohol-based film was obtained in the same manner as in Comparative Example 1, except that the polyvinyl alcohol-based resin (3) obtained in the above Synthesis Example was used, and the polyvinyl alcohol-based film that had been subjected to the drying step was peeled off from the substrate film and then heat-treated for 1 minute in a drying oven heated to 130° C. The properties of the obtained polyvinyl alcohol-based film are shown in Table 1.
- composition was prepared by blending 12 parts by mass of glycerin as a plasticizer and 0.1 parts by mass of polyoxylaurylamine as a surfactant with 100 parts by mass of the polyvinyl alcohol-based resin (4) obtained in the above Synthesis Example, and ion-exchanged water was added to the composition so that the concentration of the composition became 19% by mass.
- the composition was heated and dissolved at 130° C. for 1 hour using an autoclave to obtain an aqueous polyvinyl alcohol-based resin solution.
- This polyvinyl alcohol-based resin aqueous solution was cast onto a polyethylene terephthalate (PET) film (125 ⁇ m) as a base film so that the film thickness after drying would be 45 ⁇ m, and then dried for 7 minutes in a drying oven heated to 110° C. Thereafter, the polyvinyl alcohol-based film that had been subjected to the drying process was peeled off from the base film to obtain a polyvinyl alcohol-based film.
- the properties of the obtained polyvinyl alcohol-based film are shown in Table 1.
- Comparative Example 4 A polyvinyl alcohol-based film was obtained in the same manner as in Comparative Example 3, except that the polyvinyl alcohol-based film that had been subjected to the drying step was peeled off from the base film and then heat-treated for 1 minute in a drying oven heated to 130° C. The properties of the obtained polyvinyl alcohol-based film are shown in Table 1.
- the polyvinyl alcohol resin aqueous solution was fed to a twin-screw extruder having a vent and degassed, and then the aqueous solution temperature was set to 95°C, and the film was discharged (discharge speed 2.5 m/min, surface temperature 88°C) and cast onto a rotating cast drum from a T-shaped slit die outlet to form a film.
- the film was peeled off from the cast drum, and the front and back surfaces of the film (the surfaces in contact with the cast drum) were dried while being alternately brought into contact with a total of 15 heated rolls having a temperature range of 75°C to 100°C.
- the film was heat-treated by blowing hot air at 125°C from both sides of the film using a floating dryer. Finally, both ends were slit and wound on a roll to obtain a polyvinyl alcohol film having a thickness of 45 ⁇ m, a width of 5 m and a length of 5 km.
- the properties of the obtained polyvinyl alcohol film are shown in Table 1.
- the half-value width of the peak corresponding to polyvinyl alcohol in the differential molecular weight distribution curve of gel permeation chromatography is within the range specified in claim 1, and therefore, a polyvinyl alcohol-based film for producing a polarizing film was obtained in which the amount of polyvinyl alcohol-based resin eluted into a chemical solution containing boric acid during production of a polarizing film was small, contamination of the chemical solution tank during production of a polarizing film was suppressed, and a polarizing film with few foreign matter defects could be produced with good productivity.
- the polyvinyl alcohol-based films of Comparative Examples 1 to 5 have half-value widths of peaks corresponding to polyvinyl alcohol in differential molecular weight distribution curves of gel permeation chromatography that are outside the range specified in claim 1. This shows that a large amount of polyvinyl alcohol-based resin is eluted into a chemical solution containing boric acid during production of a polarizing plate, and the chemical solution tank is easily contaminated during production of a polarizing film.
- the polarizing film obtained by using the polyvinyl alcohol-based film of the Examples is free from foreign matter defects and has excellent polarizing properties.
- the polyvinyl alcohol-based film of the present invention for producing polarizing films is preferably used as the raw material for producing polarizing films used in liquid crystal display devices such as portable information terminals, personal computers, televisions, projectors, signage, electronic desk calculators, electronic clocks, word processors, electronic paper, game consoles, videos, cameras, photo albums, thermometers, audio equipment, instruments for automobiles and machinery, sunglasses, anti-glare glasses, stereoscopic glasses, wearable displays, foldable displays, rollable televisions, rollable displays, anti-reflection films for display elements (CRT, LCD, organic EL, electronic paper, etc.), optical communication devices, medical devices, building materials, toys, etc.
- liquid crystal display devices such as portable information terminals, personal computers, televisions, projectors, signage, electronic desk calculators, electronic clocks, word processors, electronic paper, game consoles, videos, cameras, photo albums, thermometers, audio equipment, instruments for automobiles and machinery, sunglasses, anti-glare glasses, stereoscopic glasses, wearable displays, fold
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Physics & Mathematics (AREA)
- Manufacturing & Machinery (AREA)
- Optics & Photonics (AREA)
- Health & Medical Sciences (AREA)
- Materials Engineering (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Mechanical Engineering (AREA)
- General Physics & Mathematics (AREA)
- Polarising Elements (AREA)
- Manufacture Of Macromolecular Shaped Articles (AREA)
Abstract
Description
かかる液晶表示装置には偏光膜が使用されており、偏光膜としては、主として、ポリビニルアルコール系フィルムにヨウ素を吸着配向させたものが使用されている。近年、画面の高精細化、高輝度化、大型化、薄型化にともない、従来品より一段と偏光性能に優れ、色ムラがなく、かつ幅広長尺の偏光膜が必要とされている。
特に、ホウ酸を含有する薬液中で溶出した低分子量のポリビニルアルコール系樹脂は、薬液中のヨウ素やホウ酸と会合体を形成しポリビニルアルコール系樹脂を含む異物(析出物)となる。この異物が薬液中に浮遊し加工中の偏光膜表面に付着すると、最終的に得られる偏光膜の異物欠陥となるため除去することが必要とされていた。
一方、上記特許文献2の開示技術は、バブリング装置を用いることにより、薬液槽中に発生したポリビニルアルコール系樹脂を含む異物(析出物)を効率よく除去することで長期間の連続運転を可能にし、生産効率を向上させることができるが、更なる効果を得るためには、ホウ酸を含有する処理液中におけるポリビニルアルコール系フィルムからのポリビニルアルコール系樹脂の溶出自体を抑えることが必要であった。
[1]
ゲルパーミエーションクロマトグラフィーの微分分子量分布曲線のポリビニルアルコールに対応するピークの半値幅が0.9以下であり、かつ下記条件(A)で行なうホウ酸溶液中溶出試験における溶出量が120ppm/m2以下であることを特徴とする偏光膜製造用ポリビニルアルコール系フィルム。
<条件(A)>
(i)幅50mmのポリビニルアルコール系フィルムを5枚用意し、その中の1枚のフィルムをチャック間距離40mmのチャック延伸機に取り付ける。
(ii)30℃の水浴に2分間浸漬しながら、2倍まで延伸する。
(iii)30℃のヨウ素・ヨウ化カリウム水溶液中で20秒間浸漬しながら、3倍まで延伸する。
(iv)60℃のホウ酸・ヨウ化カリウム水溶液100mL中で5分間浸漬する。
(v)残り4枚の各フィルムについても、前記(i)~(iv)の各手順を、各手順で用いた同じ水溶液中で繰り返し、前記各手順をフィルム5枚分繰り返した後の前記(iv)の溶液を溶出液とする。
(vi)前記溶出液20mLを、ホウ酸・ヨウ素・ヨウ化カリウムを含む呈色試薬20mLと混合し20℃で静置しサンプル液を調製する。
(vii)前記サンプル液について、光路長100mmの石英セルを用いてUV‐visスペクトルを取得し、690nmの吸光度を読み取る。
(viii)ポリビニルアルコール樹脂濃度既知の溶液を用いて作成した690nmの吸光度に対するポリビニルアルコール系樹脂濃度の検量線を用いて、前記溶出液中のポリビニルアルコール系樹脂濃度を算出し、溶出に使用したポリビニルアルコール系フィルムの面積で補正する。
[2]
厚みが10~50μmであることを特徴とする[1]記載の偏光膜製造用ポリビニルアルコール系フィルム。
[3]
重量膨潤度が185~200%であることを特徴とする[1]または[2]記載の偏光膜製造用ポリビニルアルコール系フィルム。
[4]
ポリビニルアルコール系樹脂の水溶液を連続的にキャスト型またはベルトに吐出および流延して製膜しフィルムを得る製膜工程と、その製膜したフィルムを105℃以上で乾燥させる乾燥工程と、その乾燥させたフィルムを熱処理する熱処理工程とを備えることを特徴とする[1]~[3]のいずれかに記載の偏光膜製造用ポリビニルアルコール系フィルムの製造方法。
[5]
[1]~[3]のいずれかに記載の偏光膜製造用ポリビニルアルコール系フィルムを用いて得られることを特徴とする偏光膜。
なお、本発明において「X~Y」(X,Yは任意の数字)と表現する場合、特にことわらない限り「X以上Y以下」の意とともに、「好ましくはXより大きい」または「好ましくはYより小さい」の意も包含する。
「X以上」(Xは任意の数字)または「Y以下」(Yは任意の数字)と表現した場合、「Xより大きいことが好ましい」または「Y未満であることが好ましい」旨の意も包含する。
本発明において「フィルム」とは、「テープ」や「シート」をも含めた意味である。
本明細書において「主成分」とは、その対象物の特性に大きな影響を与える成分の意味であり、その成分の含有量は、通常、対象物中の50質量%以上であり、好ましくは55質量%以上、より好ましくは60質量%以上、更に好ましくは70質量%以上であり、100質量%であってもよい。
また、かかる半値幅の下限は通常0.3以上であり、好ましくは0.5以上である。
かかる半値幅が0.9以下であることにより、偏光膜製造時にホウ酸を含有する薬液へのポリビニルアルコール系樹脂の溶出量が少なく、偏光膜製造時の薬液汚染を抑えることができるため、異物欠陥が少なく、生産性に優れたポリビニルアルコール系フィルムとなる。言い換えると、半値幅が上記上限値を上回ると、偏光膜製造時にホウ酸を含有する薬液にポリビニルアルコール系樹脂が多量に溶出し、薬液を汚染し、薬液中のホウ酸やヨウ化物イオンと会合体を形成することで異物欠陥が発生することとなり本発明の効果を奏しない。
また、半値幅は微分分子量分布曲線におけるdw/dlogMの最大値の半分となるlogMの幅(半値全幅)を表す。
なお、ここでいう分子量Mとは標準試料換算の分子量である。
そして、偏光膜製造用ポリビニルアルコール系フィルムのポリビニルアルコール系樹脂のゲルパーミエーションクロマトグラフィーの測定についてはフィルムを移動相等に溶解させてそのまま測定してもよいし、前処理として事前にポリビニルアルコール系樹脂以外の成分を抽出等の操作によって取り除いてから測定してもよい。
かかる下記条件(A)で行なうホウ酸溶液中溶出試験における溶出量が上記上限値以下であることにより、偏光膜製造時にホウ酸を含有する薬液へのポリビニルアルコール系樹脂の溶出量が少なく、偏光膜製造時の薬液汚染を抑えることができるため、異物欠陥が少なく、生産性に優れたポリビニルアルコール系フィルムとなる。
言い換えると、下記条件(A)で行なうホウ酸溶液中溶出試験における溶出量が上記上限値を超えると、偏光膜製造時にホウ酸を含有する薬液にポリビニルアルコール系樹脂が多量に溶出し、薬液を汚染し、薬液中のホウ酸やヨウ化物イオンと会合体を形成することで異物欠陥が発生することとなり本発明の効果を奏しない。
(i)幅50mmのポリビニルアルコール系フィルムを5枚用意し、その中の1枚のフィルムをチャック間距離40mmのチャック延伸機に取り付ける。
(ii)30℃の水浴に2分間浸漬しながら、2倍まで延伸する。
(iii)30℃のヨウ素・ヨウ化カリウム水溶液中で20秒間浸漬しながら、3倍まで延伸する。
(iv)60℃のホウ酸・ヨウ化カリウム水溶液100mL中で5分間浸漬する。
(v) 残り4枚の各フィルムについても、前記(i)~(iv)の各手順を、各手順で用いた同じ水溶液中で繰り返し、前記各手順をフィルム5枚分繰り返した後の前記(iv)の溶液を溶出液とする。
(vi) 前記得られた溶出液20mLを、ホウ酸・ヨウ素・ヨウ化カリウムを含む呈色試薬20mLと混合し20℃で静置しサンプル液を調製する。
(vii)前記サンプル液について、光路長100mmの石英セルを用いてUV‐visスペクトルを取得し、690nmの吸光度を読み取る。
(viii)ポリビニルアルコール樹脂濃度既知の溶液を用いて作成した690nmの吸光度に対するポリビニルアルコール系樹脂濃度の検量線を用いて、前記溶出液中のポリビニルアルコール系樹脂濃度を算出し、溶出に使用したポリビニルアルコール系フィルムの面積で補正する。
工程(A):ポリビニルアルコール系樹脂水溶液を調液する工程。
工程(B):ポリビニルアルコール系樹脂の水溶液をキャスト型に流延して製膜する工程。
工程(C):製膜されたフィルムを乾燥する工程。
工程(D):得られたフィルムを熱処理する工程。
工程(A)ポリビニルアルコール系樹脂水溶液を調液する工程(調液工程)である。
まず、上記ポリビニルアルコール系フィルムの材料であるポリビニルアルコール系樹脂、およびポリビニルアルコール系樹脂水溶液に関して説明する。
本実施形態において、ポリビニルアルコール系フィルムを構成するポリビニルアルコール系樹脂としては、通常、未変性のポリビニルアルコール系樹脂、すなわち、酢酸ビニルを重合して得られるポリ酢酸ビニルをケン化して製造される樹脂が用いられる。必要に応じて、酢酸ビニルと、少量(通常10モル%以下、好ましくは5モル%以下)の酢酸ビニルと共重合可能な成分との共重合体をケン化して得られる樹脂を用いることもできる。酢酸ビニルと共重合可能な成分としては、例えば、不飽和カルボン酸(例えば、塩、エステル、アミド、ニトリル等を含む)、炭素数2~30のオレフィン類(例えば、エチレン、プロピレン、n-ブテン、イソブテン等)、ビニルエーテル類、不飽和スルホン酸塩等が挙げられる。また、ケン化後の水酸基を化学修飾して得られる変性ポリビニルアルコール系樹脂を用いることもできる。これらは単独でもしくは2種以上併せて用いることができる。
かかる分散度が小さすぎるとポリビニルアルコール系フィルムを用いて偏光膜を製造する際に、延伸が困難となる傾向があり、大きすぎるとポリビニルアルコール系樹脂を光学フィルムとする場合に十分な光学性能が得られにくい傾向がある。
なお、上記ポリビニルアルコール系樹脂の分散度測定時の重量平均分子量、数平均分子量は、GPC法により測定される重量平均分子量、数平均分子量である。
ここで、本発明における平均ケン化度は、JIS K 6726に準じて測定されるものである。
工程(B)はポリビニルアルコール系樹脂の水溶液をキャスト型に流延して製膜する工程(製膜工程)である。
上記脱泡処理の後、ポリビニルアルコール系樹脂水溶液は、一定量ずつT型スリットダイに導入され、回転するキャストドラム上に吐出および流延されて、連続キャスト法によりフィルムに製膜される。
かかるポリビニルアルコール系樹脂水溶液の樹脂温度が低すぎると流動不良となる傾向があり、高すぎると発泡する傾向がある。
かかる水溶液の粘度が、高すぎると流動不良となる傾向があり、低すぎると流延製膜が困難となる傾向がある。
かかる吐出速度が遅すぎると生産性が低下する傾向があり、速すぎると流延が困難となる傾向がある。
かかる直径が小さすぎるとキャストドラム上での乾燥区間が短くなることから速度が上がりにくい傾向があり、大きすぎると輸送性が低下する傾向がある。
キャストドラムの幅が小さすぎると生産性が低下する傾向がある。
かかる回転速度が遅すぎると生産性が低下する傾向があり、速すぎると乾燥が不十分となる傾向がある。
工程(C)は上記製膜されたフィルムを乾燥する工程(乾燥工程)である。
本実施形態においては、かかる乾燥工程におけるフィルムの乾燥方法としては特に限定されるものではなく、熱ロールを用いて乾燥させる方法、乾燥炉内で乾燥させる方法等を用いて乾燥させればよい。
また、乾燥温度の上限値としては、通常150℃以下であり、好ましくは140℃以下、特に好ましくは135℃以下、更に好ましくは130℃以下、最も好ましくは125℃以下である。
かかる乾燥温度が低すぎると乾燥不良となる傾向があり、高すぎると乾燥しすぎることとなり、うねり等の外観不良を招く傾向がある。
乾燥時間が長くなりすぎると偏光膜製造時の染色性が低下する傾向があり、短すぎると乾燥不良となる傾向がある。
熱ロール乾燥時間が長くなりすぎると偏光膜製造時の染色性が低下する傾向があり、速くなりすぎると偏光膜製造時の膨潤工程でフィルムがシワや折れが発生しやすくなり、偏光膜の外観が低下する傾向がある。
工程(D)は得られたフィルムを熱処理する工程(熱処理工程)である。
上記工程(C)を経たフィルムを、例えば、乾燥炉、フローティングドライヤー等で熱処理を行なえばよい。
かかる熱処理の温度とは、例えば、乾燥炉内で熱処理する場合には乾燥炉内の温度をいい、フローティングドライヤーで熱処理する場合にはフローティングドライヤー内の温度をいう。熱処理の温度は、上限が140℃以下であることが好ましく、特に好ましくは135℃以下、更に好ましくは130℃以下、殊に好ましくは125℃以下である。また下限が60℃以上であることが好ましく、特に好ましくは75℃以上、更に好ましくは105℃以上、殊に好ましくは110℃以上である。
熱処理温度が高すぎると偏光膜製造時の染色性が低下する傾向があり、低くすぎると偏光膜製造時の膨潤工程でフィルムがシワや折れが発生しやすくなり、偏光膜の外観が低下する傾向がある。
また、熱処理時間は20~100秒間であることが好ましく、特に好ましくは40~70秒間である。
かくして上記工程(A)~(D)を経てポリビニルアルコール系フィルムが得られ、最終的にロールに巻き取られて製品となる。
かかる重量膨潤度が上記範囲より低いと偏光膜作製時における延伸性が低下する傾向があり、上記範囲を超えると延伸性は良くなるが偏光膜の偏光性能が低下する傾向がある。
かかる弾性率が低すぎると薄型の偏光膜製造時に破断が生じやすい傾向があり、高すぎると偏光膜製造時の延伸性が低下する傾向がある。
かかる水中への溶出量が上記範囲内にあることにより、偏光膜製造時に水中へのポリビニルアルコール系樹脂の溶出量が少なく、偏光膜製造時の薬液汚染を抑えることができるため、異物欠陥が少なく、生産性に優れたポリビニルアルコール系フィルムとなる。
水中の溶出量は、例えば、後記実施例に記載の方法で測定することができる。
本発明の一実施形態に係る偏光膜は、本実施形態の製造方法により得られた上記ポリビニルアルコール系フィルムを、ロールから繰り出して水平方向に移送し、膨潤、染色、ホウ酸架橋、延伸、洗浄、乾燥等の工程を経て製造される。
なお、偏光度は、一般的に2枚の偏光膜を、その配向方向が同一方向になるように重ね合わせた状態で、波長λにおいて測定した光線透過率(H11)と、2枚の偏光膜を、配向方向が互いに直交する方向になる様に重ね合わせた状態で、波長λにおいて測定した光線透過率(H1)より、下記式(1)にしたがって算出される。
偏光度=〔(H11-H1)/(H11+H1)〕1/2 ・・・(1)
単体透過率は、分光光度計を用いて偏光膜単体の光線透過率を測定して得られる値である。
本実施形態の偏光膜は、色ムラが少なく、偏光性能に優れた偏光板を製造するのに好適である。
偏光板は、本実施形態の偏光膜の片面または両面に、接着剤を介して、光学的に等方性な樹脂フィルムを保護フィルムとして貼合することにより、作製される。保護フィルムとしては、例えば、トリアセチルセルロースやジアセチルセルロースのようなアセチルセルロース系樹脂からなるフィルム、ポリエチレンテレフタレート、ポリエチレンナフタレートおよびポリブチレンテレフタレートのようなポリエステル系樹脂からなるフィルム、ポリカーボネート系樹脂フィルム、シクロオレフィン系樹脂フィルム、アクリル系樹脂フィルム、ポリプロピレン系樹脂の鎖状オレフィン系樹脂からなるフィルムが挙げられる。
なお、例中「部」、「%」とあるのは、質量基準を意味する。
<GPC測定>
ポリビニルアルコール系フィルム0.8gから下記条件の高速溶媒抽出で可塑剤と界面活性剤を除去したものを測定サンプルとして用い、ゲルパーミエーションクロマトグラフィー(GPC)にて下記の測定条件で測定してクロマトグラムを得た。標準ポリエチレンオキサイドおよびポリエチレングリコール(PEO/PEG)を測定して得られた検量線を用いて、このときの溶出時間を分子量に換算して、ポリビニルアルコール系フィルムの標準試料(PEO/PEG)換算の重量平均分子量と分子量分布(Mw/Mn)と微分分子量分布曲線を得た。また、微分分子量分布曲線からポリビニルアルコールに対応するピークの半値幅を算出した。
[高速溶媒抽出の条件]
・装置:ダイオネクス社製 ASE-20 (11mLセル)
・抽出溶媒:メタノール/水=90/10
・昇温時間:5min
・抽出圧力/静置時間:1500psi/10min
・フラッシュ量:80%
・パージ時間:60sec
・サイクル:2cycle
・抽出回数:2回
[GPCの測定条件]
・GPC装置:島津製作所社製 Prominence
・検出器:RI、Shodex RI-501
・カラム:東ソー社製のTSKgel α-M 13μm 7.8mm I.D.×30cmを用いた。
・移動相:0.2M NaNO3水溶液
・移動相流量:0.50mL/分
・カラム温度:35℃
・検量線:分子量が異なる12種類のPEO/PEG標準サンプルを用いて検量線を作成した。
ポリビニルアルコール系フィルムを100mm×100mmに切り出し、30℃に調整したイオン交換水槽に15分間浸漬した。浸漬後にフィルムを取り出し、濾紙(5A)上にフィルムを広げて置き、更に濾紙(5A)をフィルムの上に重ね、その上に150mm×150mm×4mm(4.4g/cm2)のSUS板を5秒間載せ、フィルム表面の付着水を除去した。このフィルムを速やかに秤量瓶に入れ、重量を測定し、これを膨潤時のフィルム重量Aとした。上記操作は23℃、50%RHの環境にて行った。次に、該フィルムを160℃の乾燥機に10分間静置し、乾燥材を入れたデシケータ内で5分間放冷し、フィルム中の水分を除去した。その後フィルムを取り出し、速やかに秤量瓶に入れ、重量を測定し、これを乾燥後のフィルム重量Bとした。そして、膨潤時のフィルム重量Aと乾燥後のフィルム重量Bを基に重量膨潤度を下式より求めた。
重量膨潤度(%)=A/B×100
[試験方法]
(i)幅50mm×長さ100mmのポリビニルアルコール系フィルムを5枚用意し、その中の1枚のフィルムを、サイズ横100mm×縦25mmのチャック部に、フィルム幅50mm×チャック間距離40mmとなるようにチャック延伸機に取り付け、(ii)30℃の水浴に2分間浸漬しながら総延伸倍率2倍まで延伸した。次に、(iii)ヨウ素0.5g/L、ヨウ化カリウム2.5g/Lを含む30℃の水溶液に20秒間浸漬しながら総延伸倍率3倍まで延伸し、ポリビニルアルコール系フィルムをチャック部で切断して染色されたポリビニルアルコール系フィルムを得た。(iv)染色されたポリビニルアルコール系フィルムをホウ酸44g/L、ヨウ化カリウム120g/Lを含む60℃の水溶液100mL中に5分間浸漬し、溶出液を得た。(v)残り4枚の各フィルムについても、前記(i)~(iv)の各手順を、各手順で用いた同一の薬液中で繰り返し、前記各手順をフィルム5枚分繰り返した後の前記(iv)の溶液(「ホウ酸液」という場合がある)を、測定用の溶出液として得た。
(vi)得られた測定用の溶出液20mLと、呈色試薬(イオン交換水500g、ヨウ化カリウム7.4g、ヨウ素0.65g、ホウ酸10.6gからなる試薬)20mLとを室温(23℃)で混合したのち、20℃で15分間静置しサンプル液を調製した。(vii)前記サンプル液について、分光光度計(島津製作所社製UV-3600Plus)と光路長100mmの石英セルとを用いて波長690nmの吸光度を測定した。(viii)あらかじめ作成した検量線を用いて、前記溶出液中のポリビニルアルコール系樹脂の濃度(ppm)を算出し、溶出に用いたフィルムの総面積を50mm×40mm×5枚=0.01m2として算出し、得られたポリビニルアルコール系樹脂の濃度(ppm)を面積換算してホウ酸液中の溶出量(ppm/m2)とした。
[評価]
〇(Good) : 120ppm/m2以下
×(Poor) : 120ppm/m2より大きい
[検量線の作成]
ポリビニルアルコール系樹脂に、ポリビニルアルコール系樹脂の純分が200ppmとなるようにイオン交換水を加え、オートクレーブを用いて130℃にて1時間加熱溶解し、標準溶液を得た。標準溶液をイオン交換水で希釈してポリビニルアルコール系樹脂の濃度が20ppm、10ppm、5ppm、2ppm、1ppm、0.5ppm、0.2ppm、0.1ppmの各ポリビニルアルコール系樹脂水溶液を得た。各濃度の水溶液20mLと呈色試薬(イオン交換水500g、ヨウ化カリウム7.4g、ヨウ素0.65g、ホウ酸10.6gからなる試薬)20mLとを室温で混合したのち、20℃で15分間静置し、分光光度計(島津製作所社製UV-3600Plus)と光路長100mmの石英セルを用いて波長690nmの吸光度を測定し、690nmの吸光度に対するポリビニルアルコール系樹脂濃度(ppm)をプロットして検量線を作成した。
[試験方法]
得られたポリビニルアルコール系フィルムを、23℃50%RHで24時間調湿した後、100mm×100mm(0.01m2)の試験片を5枚切り出し、当該試験片を1枚ずつ50℃のイオン交換水1Lに1分間浸漬する操作を5枚分繰り返して溶出液を得た。かかる溶出液10mLに呈色試薬(イオン交換水500g、ヨウ化カリウム7.4g、ヨウ素0.65g、ホウ酸10.6gからなる試薬)10mLを室温で混合した後、分光光度計(島津製作所社製UV-3600Plus)を用いて波長690nmの吸光度を測定し、あらかじめ作成した検量線からポリビニルアルコール系樹脂の濃度(ppm)を算出し、面積換算することで水中の溶出量(ppm/m2)とした。
[評価]
〇(Good) : 溶出量が900ppm/m2以下
×(Poor) : 溶出量が900ppm/m2より大きい
[試験方法]
ホウ酸液中の溶出量試験で得られた溶出液を室温で24時間静置したのち、析出物の有無を目視で確認した。
[評価]
◎(Excellent): 析出物が視認されなかった
〇(Good): 析出物がわずかに視認された
×(Poor): 多量の析出物が視認された
得られたポリビニルアルコール系フィルムから長さ120mm×幅15mmの試験片を切り出し、23℃40%RHの恒温恒湿器中で24時間以上調湿した後、島津製作所社製「精密万能試験機、オートグラフ(AG-IS)」を用いて 、JIS K7127:1999(引っ張り速度1000mm/分、チャック間距離50mm)に準じて、23℃40%RHの環境下で長さ方向に引張試験を実施し、弾性率(N/mm2)を得た。
<合成例1>
還流冷却管、試料投入口、窒素導入口、撹拌翼を備えた反応器に酢酸ビニル800質量部とコバルト(II)アセチルアセトナート0.32質量部を加えて窒素バブリングを30分間行い、反応器内を窒素置換するとともに液内の溶存酸素を追い出した。その後、反応器を水浴に浸漬して40℃に加温して、そこに開始剤として2,2'-アゾビス(4-メトキシ-2,4-ジメチルバレロニトリル)1.04質量部を添加した。開始剤を添加してから2時間後に降温し、内温を30℃に維持して重合を開始した。なお、開始剤を添加してから2時間の間は重合が進行しない誘導期であった。適宜サンプリングを行い、その固形分濃度から重合の進行を確認し、酢酸ビニルの転化率が35%に到達したところで重合停止剤として1,1-ジフェニルエチレン1.04質量部を添加して、30℃を維持したまま30分間撹拌した。開始剤を添加してから目標転化率に至るまでに7時間を要した。
重合停止剤を加えてから30分後に更に反応器に酢酸4質量部とメタノール160質量部を加えて30分間撹拌を継続した。そこに、精製水を添加してポリ酢酸ビニルを析出させて上澄み液を除去して、ポリ酢酸ビニルを水洗した。得られたポリ酢酸ビニルはメタノールに溶解させたのちに、減圧下でメタノールと酢酸ビニルと水を留去した。適宜、粘度が上昇したところでメタノールを添加して残存する酢酸ビニルを追い出してポリ酢酸ビニルのメタノール溶液を得た。
このようにして得られたポリ酢酸ビニルのメタノール溶液を濃度3.5質量%になるまでメタノールで希釈して、上記同様の反応器に仕込んだ。この反応器を水浴に浸漬して内温が50℃となるように加温した。そこに3.6質量%の水酸化ナトリウムのメタノール溶液を120質量部添加して、ケン化反応を開始した。ケン化反応が進むとケン化物が析出するが、そのまま撹拌を継続した。水酸化ナトリウムのメタノール溶液を添加してから2時間後に得られたケン化物を濾別して、再度反応器に仕込み、そこにメタノールを500質量部添加して50℃に加温した。そこに3.6質量%の水酸化ナトリウムのメタノール溶液180質量部を添加して3時間反応させることで、ケン化反応を追い込んだ。その後、酢酸を4.2質量部を添加して中和を行い、メタノールで洗浄しながら吸引ろ過し、ケン化物を得た。得られたケン化物100質量部に対して、メタノール500質量部を加えて50℃で30分間洗浄して濾別する操作を2度行った。洗浄後のケン化物は真空乾燥機で50℃で12時間乾燥させ、ポリビニルアルコール系樹脂(1)(重量平均分子量73400;ケン化度99.8モル%;Mw/Mn=2.07;微分分子量曲線の半値幅0.70)を得た。
還流冷却管、試料投入口、撹拌翼を備えた反応器に酢酸ビニル650質量部とメタノール131質量部を加えて、反応器を水浴に浸漬して昇温した。冷却管からの還流が見られたところ(内温が60℃程度)で、開始剤として2,2'-アゾビス(イソブチロニトリル)0.052質量部を添加した。重合中は冷却管からの還流が継続するように適宜水浴の温度を調整するとともに、サンプリングを行い、その固形分濃度から重合の進行を確認し、酢酸ビニルの転化率が50%に到達したところで重合停止剤としてm-ジニトロベンゼン0.013質量部とメタノール500質量部を添加して重合を終了した。開始剤を添加してから目標転化率に至るまでに5時間を要した。
得られた重合後の溶液は減圧下でメタノールと酢酸ビニルを留去した。適宜、粘度が上昇したところでメタノールを添加して残存する酢酸ビニルを追い出してポリ酢酸ビニルのメタノール溶液を得た。
以降の合成工程は合成例1と同様の方法によりポリビニルアルコール系樹脂(2)(重量平均分子量79000;ケン化度99.8モル%;Mw/Mn=2.27;微分分子量曲線の半値幅0.95)を得た。
還流冷却管、試料投入口、撹拌翼を備えた反応器に酢酸ビニル650質量部とメタノール85質量部を加えて、反応器を水浴に浸漬して昇温した。冷却管からの還流が見られたところ(内温が60℃程度)で、開始剤として2,2'-アゾビス(イソブチロニトリル)0.13質量部を添加した。重合中は冷却管からの還流が継続するように適宜水浴の温度を調整するとともに、サンプリングを行い、その固形分濃度から重合の進行を確認し、酢酸ビニルの転化率が70%に到達したところで重合停止剤としてm-ジニトロベンゼン0.033質量部とメタノール500質量部を添加して重合を終了した。開始剤を添加してから目標転化率に至るまでに3.5時間を要した。
以降の合成工程は合成例1と同様の方法によりポリビニルアルコール系樹脂(3)(重量平均分子量79700;ケン化度99.8モル%;Mw/Mn=2.36;微分分子量曲線の半値幅0.97)を得た。
還流冷却管、試料投入口、撹拌翼を備えた反応器に酢酸ビニル650質量部とメタノール65質量部を加えて、反応器を水浴に浸漬して昇温した。冷却管からの還流が見られたところ(内温が60℃程度)で、開始剤として2,2'-アゾビス(イソブチロニトリル)0.0325質量部を添加した。重合中は冷却管からの還流が継続するように適宜水浴の温度を調整するとともに、サンプリングを行い、その固形分濃度から重合の進行を確認し、酢酸ビニルの転化率が50%に到達したところで重合停止剤としてm-ジニトロベンゼン0.01質量部とメタノール500質量部を添加して重合を終了した。開始剤を添加してから目標転化率に至るまでに5時間を要した。
以降の合成工程は合成例2と同様の方法によりポリビニルアルコール系樹脂(4)(重量平均分子量101000;ケン化度99.8モル%;Mw/Mn=2.42;微分分子量曲線の半値幅0.92)を得た。
<ポリビニルアルコール系フィルムの作製]
上記合成例で得られたポリビニルアルコール系樹脂(1)100質量部に対して、可塑剤としてグリセリン12質量部、界面活性剤としてポリオキシラウリルアミン0.1質量部を配合した組成物に、前記組成物の濃度が19質量%となるようにイオン交換水を加え、オートクレーブを用いて130℃にて1時間加熱溶解し、ポリビニルアルコール系樹脂水溶液を得た。
このポリビニルアルコール系樹脂水溶液を基材フィルムとしてポリエチレンテレフタラート(PET)フィルム(膜厚125μm)上に乾燥後のフィルム膜厚が45μmとなるように連続的に流延し、110℃に加熱した乾燥炉で7分間乾燥した。その後、基材フィルムから乾燥工程を経たポリビニルアルコール系フィルムを剥離し、120℃の乾燥炉で1分間熱処理することでポリビニルアルコール系フィルムを得た。
得られたポリビニルアルコール系フィルムの特性を表1に示す。
乾燥工程を経たポリビニルアルコール系フィルムを基材フィルムから剥離後、乾燥炉での熱処理温度を130℃に変更した以外は実施例1と同様の手順でポリビニルアルコール系フィルムを得た。得られたポリビニルアルコール系フィルムの特性を表1に示す。
上記合成例で得られたポリビニルアルコール系樹脂(2)100質量部に対して、可塑剤としてグリセリン12質量部、界面活性剤としてポリオキシラウリルアミン0.1質量部を配合した組成物に、前記組成物の濃度が19質量%となるようにイオン交換水を加え、オートクレーブを用いて130℃にて1時間加熱溶解し、ポリビニルアルコール系樹脂水溶液を得た。
このポリビニルアルコール系樹脂水溶液を基材フィルムとしてポリエチレンテレフタラート(PET)フィルム(125μm)上に乾燥後のフィルム膜厚が45μmとなるように流延し、110℃に加熱した乾燥炉で7分間乾燥した。その後、基材フィルムから乾燥工程を経たポリビニルアルコール系フィルムを剥離して、ポリビニルアルコール系フィルムを得た。
得られたポリビニルアルコール系フィルムの特性を表1に示す。
上記合成例で得られたポリビニルアルコール系樹脂(3)を使用し、乾燥工程を経たポリビニルアルコール系フィルムを基材フィルムから剥離後、130℃に加熱した乾燥炉で1分間熱処理したこと以外は比較例1と同様の手順でポリビニルアルコール系フィルムを得た。得られたポリビニルアルコール系フィルムの特性を表1に示す。
上記合成例で得られたポリビニルアルコール系樹脂(4)100質量部に対して、可塑剤としてグリセリン12質量部、界面活性剤としてポリオキシラウリルアミン0.1質量部を配合した組成物に、前記組成物の濃度が19質量%となるようにイオン交換水を加え、オートクレーブを用いて130℃にて1時間加熱溶解し、ポリビニルアルコール系樹脂水溶液を得た。
このポリビニルアルコール系樹脂水溶液を基材フィルムとしてポリエチレンテレフタラート(PET)フィルム(125μm)上に乾燥後のフィルム膜厚が45μmとなるように流延し、110℃に加熱した乾燥炉で7分間乾燥した。その後、基材フィルムから乾燥工程を経たポリビニルアルコール系フィルムを剥離して、ポリビニルアルコール系フィルムを得た。得られたポリビニルアルコール系フィルムの特性を表1に示す。
乾燥工程を経たポリビニルアルコール系フィルムを基材フィルムから剥離後、130℃に加熱した乾燥炉で1分間熱処理したこと以外は比較例3と同様の手順でポリビニルアルコール系フィルムを得た。得られたポリビニルアルコール系フィルムの特性を表1に示す。
上記合成例で得られたポリビニルアルコール系樹脂(4)100質量部に対して、可塑剤としてグリセリン12質量部、界面活性剤としてポリオキシラウリルアミン0.1質量部を配合した組成物に、前記組成物の濃度が29質量%となるようにイオン交換水を加え、撹拌しながら140℃まで昇温して加圧溶解した後、均一に溶解したポリビニルアルコール系樹脂水溶液を得た。次に該ポリビニルアルコール系樹脂水溶液を、ベントを有する2軸押出機に供給して脱泡した後、水溶液温度を95℃にし、T型スリットダイ吐出口より、回転するキャストドラムに吐出(吐出速度2.5m/分、表面温度88℃)および流延して製膜した。キャストドラムからフィルムを剥離し、フィルムの表面と裏面(キャストドラムとの接触面)とを75℃から100℃の温度範囲にある合計15本の熱ロールに交互に接触させながら乾燥させた。次いで、フローティングドライヤーを用いて、フィルム両面から125℃の熱風を吹き付けて熱処理を行なった。最後に、両端部をスリットしてロールに巻き取り、厚み45μm、幅5m、長さ5kmのポリビニルアルコール系フィルムを得た。得られたポリビニルアルコール系フィルムの特性を表1に示す。
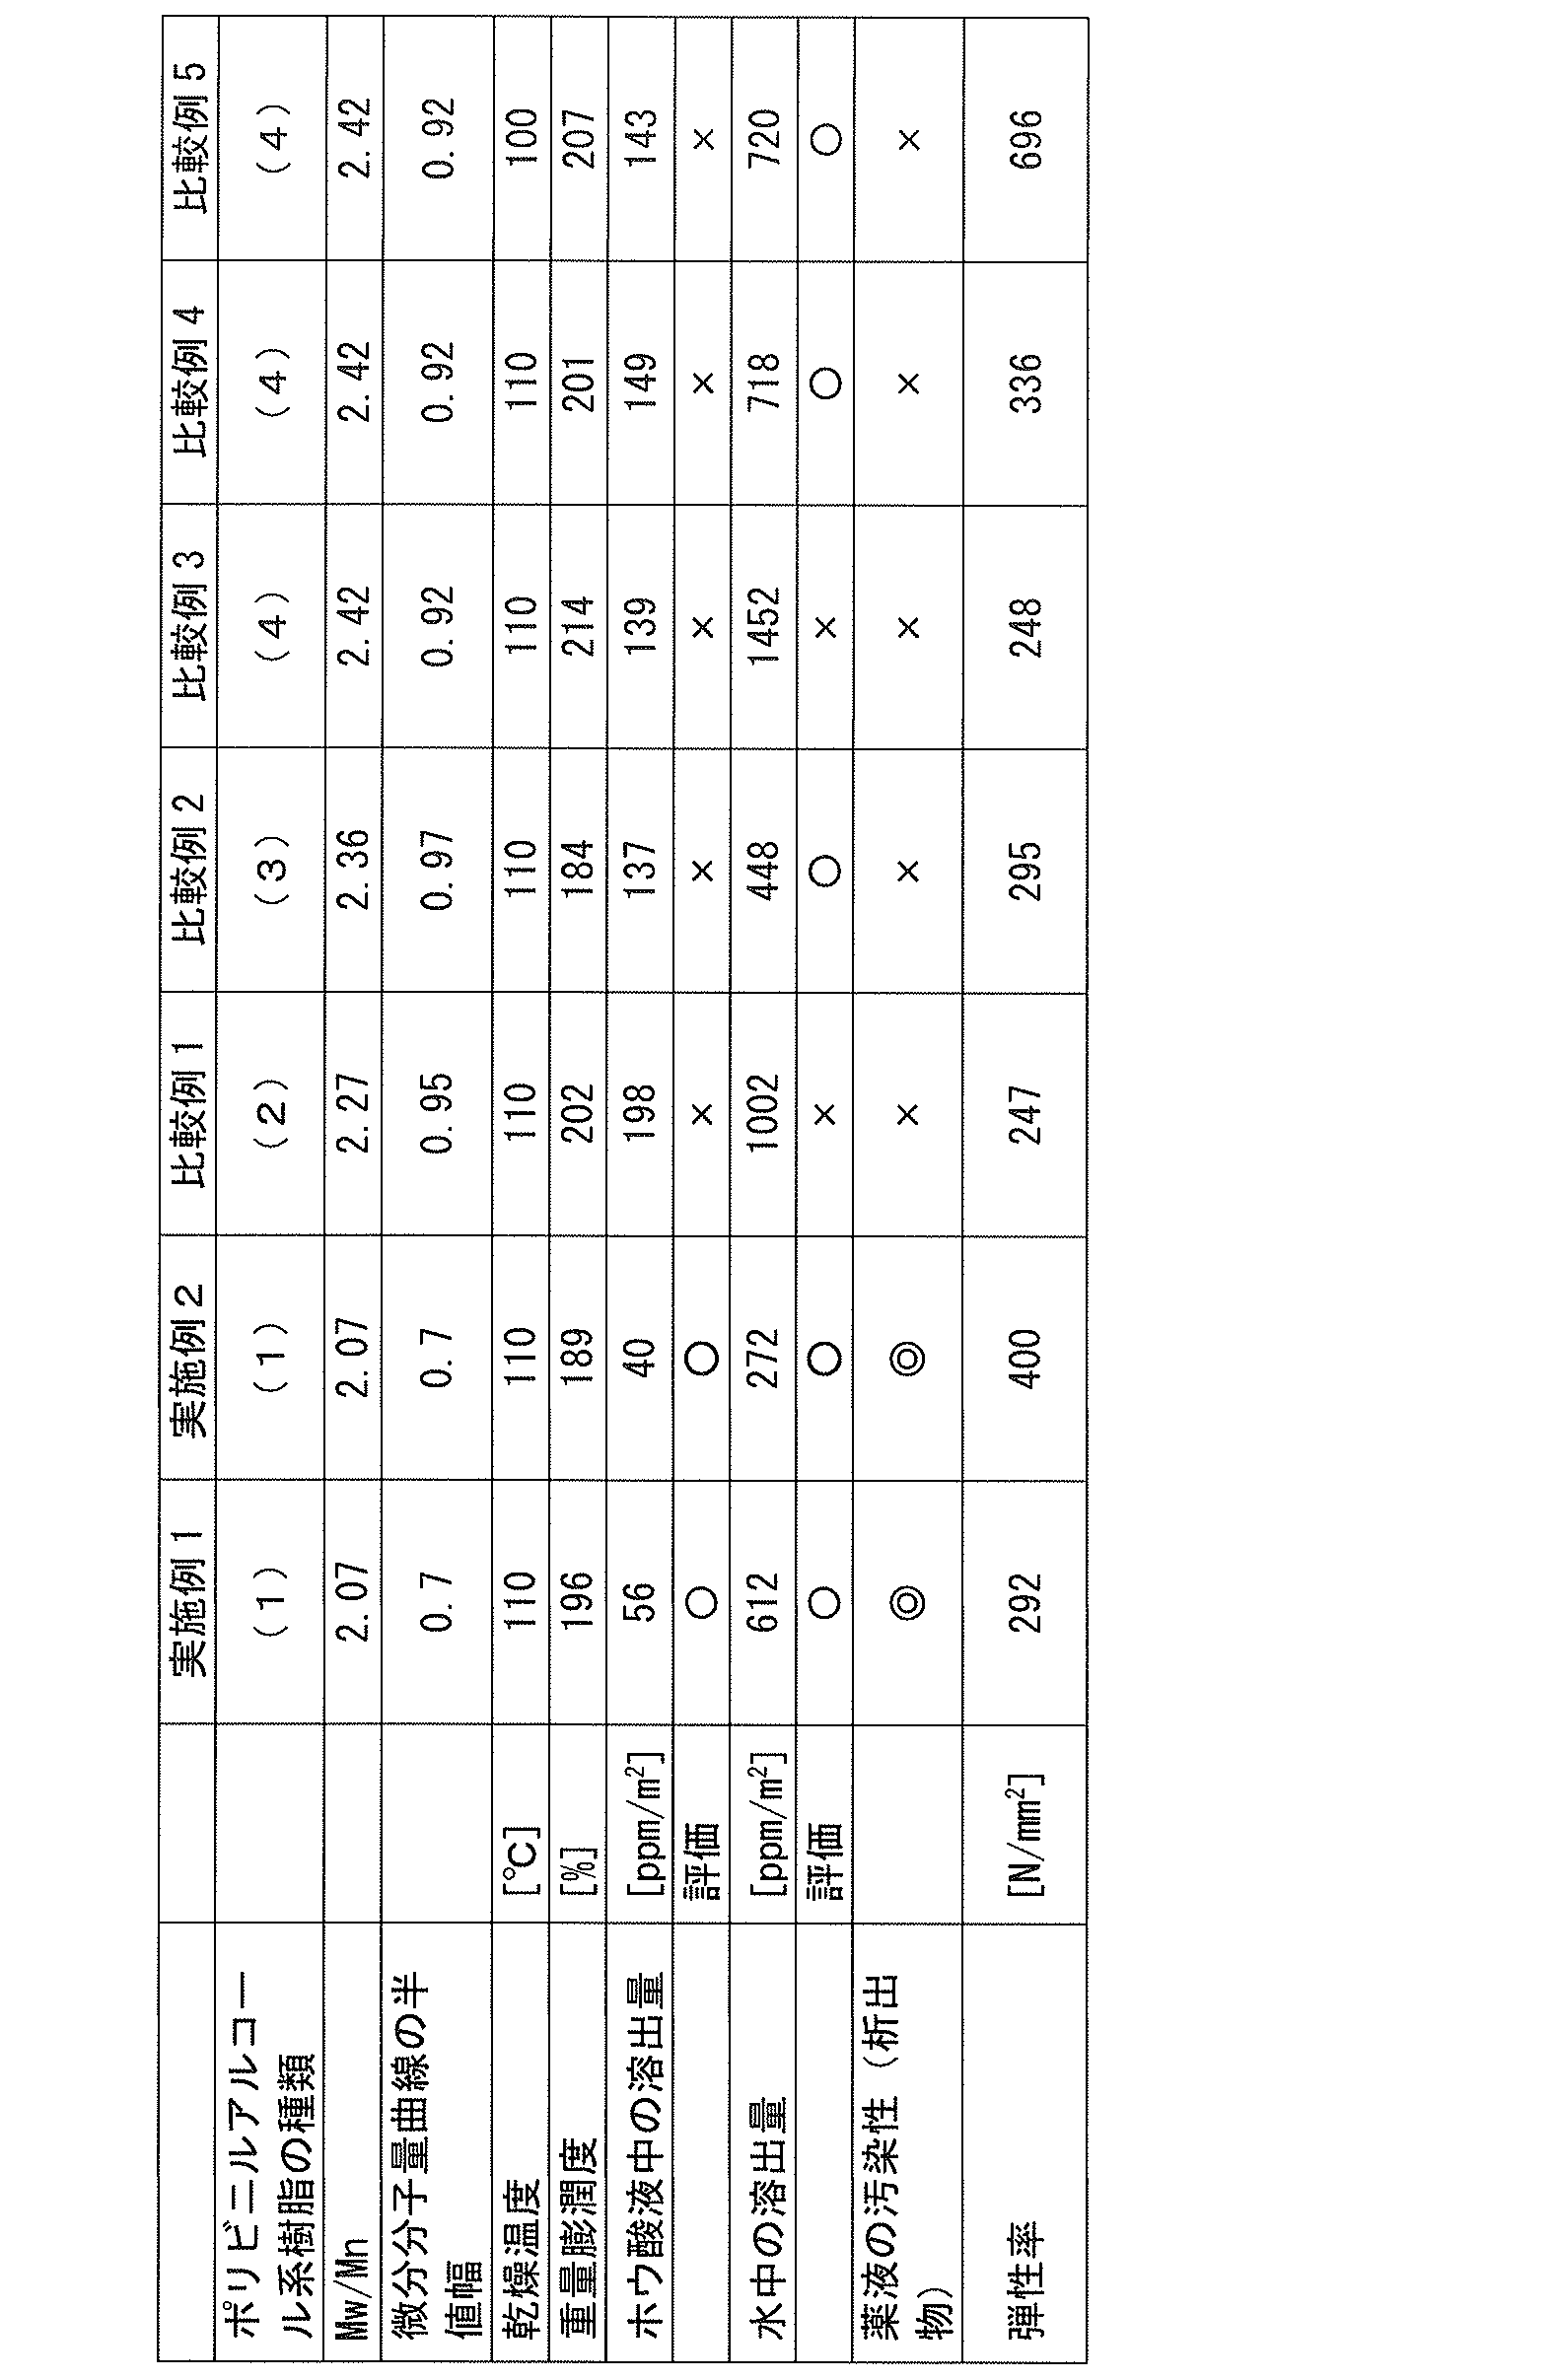
それに対し、比較例1~5のポリビニルアルコール系フィルムは、ゲルパーミエーションクロマトグラフィーの微分分子量分布曲線のポリビニルアルコールに対応するピークの半値幅が請求項1で特定する範囲外であるため、偏光板製造時にホウ酸を含有する薬液へのポリビニルアルコール系樹脂の溶出量が多く、偏光膜製造時の薬液槽が汚染されやすいことがわかる。
なお、実施例のポリビニルアルコール系フィルムを用いて得られる偏光膜は、異物欠陥がなく、偏光性能に優れたものである。
Claims (5)
- ゲルパーミエーションクロマトグラフィーの微分分子量分布曲線のポリビニルアルコールに対応するピークの半値幅が0.9以下であり、かつ下記条件(A)で行なうホウ酸溶液中溶出試験における溶出量が120ppm/m2以下であることを特徴とする偏光膜製造用ポリビニルアルコール系フィルム。
<条件(A)>
(i)幅50mmのポリビニルアルコール系フィルムを5枚用意し、その中の1枚のフィルムをチャック間距離40mmのチャック延伸機に取り付ける。
(ii)30℃の水浴に2分間浸漬しながら、2倍まで延伸する。
(iii)30℃のヨウ素・ヨウ化カリウム水溶液中で20秒間浸漬しながら、3倍まで延伸する。
(iv)60℃のホウ酸・ヨウ化カリウム水溶液100mL中で5分間浸漬する。
(v)残り4枚の各フィルムについても、前記(i)~(iv)の各手順を、各手順で用いた同じ水溶液中で繰り返し、前記各手順をフィルム5枚分繰り返した後の前記(iv)の溶液を溶出液とする。
(vi)前記溶出液20mLを、ホウ酸・ヨウ素・ヨウ化カリウムを含む呈色試薬20mLと混合し20℃で静置しサンプル液を調製する。
(vii)前記サンプル液について、光路長100mmの石英セルを用いてUV‐visスペクトルを取得し、690nmの吸光度を読み取る。
(viii)ポリビニルアルコール樹脂濃度既知の溶液を用いて作成した690nmの吸光度に対するポリビニルアルコール系樹脂濃度の検量線を用いて、前記溶出液中のポリビニルアルコール系樹脂濃度を算出し、溶出に使用したポリビニルアルコール系フィルムの面積で補正する。 - 厚みが10~50μmであることを特徴とする請求項1記載の偏光膜製造用ポリビニルアルコール系フィルム。
- 重量膨潤度が185~200%であることを特徴とする請求項1または2記載の偏光膜製造用ポリビニルアルコール系フィルム。
- ポリビニルアルコール系樹脂の水溶液を連続的にキャスト型またはベルトに吐出および流延して製膜しフィルムを得る製膜工程と、その製膜したフィルムを105℃以上で乾燥させる乾燥工程と、その乾燥させたフィルムを熱処理する熱処理工程とを備えることを特徴とする請求項1または2記載の偏光膜製造用ポリビニルアルコール系フィルムの製造方法。
- 請求項1または2記載の偏光膜製造用ポリビニルアルコール系フィルムを用いて得られることを特徴とする偏光膜。
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020257008254A KR20250124293A (ko) | 2022-12-26 | 2023-12-25 | 편광막 제조용 폴리비닐 알코올계 필름 및 이의 제조 방법, 및 이를 이용하여 이루어진 편광막 |
| CN202380065464.8A CN119866460A (zh) | 2022-12-26 | 2023-12-25 | 偏光膜制造用聚乙烯醇系薄膜及其制造方法、以及使用其而成的偏光膜 |
| JP2024567771A JPWO2024143239A1 (ja) | 2022-12-26 | 2023-12-25 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2022-207791 | 2022-12-26 | ||
| JP2022207791 | 2022-12-26 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2024143239A1 true WO2024143239A1 (ja) | 2024-07-04 |
Family
ID=91717883
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2023/046305 Ceased WO2024143239A1 (ja) | 2022-12-26 | 2023-12-25 | 偏光膜製造用ポリビニルアルコール系フィルムおよびその製造方法、並びにそれを用いてなる偏光膜 |
Country Status (5)
| Country | Link |
|---|---|
| JP (1) | JPWO2024143239A1 (ja) |
| KR (1) | KR20250124293A (ja) |
| CN (1) | CN119866460A (ja) |
| TW (1) | TW202438581A (ja) |
| WO (1) | WO2024143239A1 (ja) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2024169407A (ja) * | 2023-05-24 | 2024-12-05 | 長春石油化學股▲分▼有限公司 | ポリビニルアルコールフィルム及びこれから製造された光学フィルム |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4289815A (en) * | 1978-06-26 | 1981-09-15 | Airwick Industries, Inc. | Cold water-insoluble polyvinyl alcohol pouch for the controlled release of active ingredients |
| WO2016060097A1 (ja) * | 2014-10-16 | 2016-04-21 | 日本合成化学工業株式会社 | ポリビニルアルコール系フィルムおよびその製造方法、並びに偏光フィルム、偏光板 |
| WO2017033552A1 (ja) * | 2015-08-26 | 2017-03-02 | 日本合成化学工業株式会社 | 偏光膜製造用ポリビニルアルコール系樹脂、およびその製造方法、ポリビニルアルコール系フィルムおよびその製造方法、偏光膜、ポリビニルアルコール系樹脂 |
| JP2018010281A (ja) * | 2016-06-29 | 2018-01-18 | 日本合成化学工業株式会社 | ポリビニルアルコール系フィルム、およびその製造方法、ならびに偏光膜 |
| WO2022138720A1 (ja) * | 2020-12-23 | 2022-06-30 | 三菱ケミカル株式会社 | 偏光膜製造用ポリビニルアルコール系フィルム、偏光膜製造用ポリビニルアルコール系フィルムの製造方法、偏光膜 |
| WO2022202861A1 (ja) * | 2021-03-24 | 2022-09-29 | 三菱ケミカル株式会社 | ポリビニルアルコール系フィルム、およびその製造方法、ならびにそれを用いた偏光膜、偏光板 |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5479752B2 (ja) | 2008-02-19 | 2014-04-23 | 株式会社クラレ | ビニルアルコール系重合体およびその製造方法 |
| JP7490500B2 (ja) | 2019-09-12 | 2024-05-27 | 住友化学株式会社 | ポリビニルアルコール除去装置及び偏光子の製造方法 |
-
2023
- 2023-12-25 WO PCT/JP2023/046305 patent/WO2024143239A1/ja not_active Ceased
- 2023-12-25 CN CN202380065464.8A patent/CN119866460A/zh active Pending
- 2023-12-25 JP JP2024567771A patent/JPWO2024143239A1/ja active Pending
- 2023-12-25 KR KR1020257008254A patent/KR20250124293A/ko active Pending
- 2023-12-25 TW TW112150485A patent/TW202438581A/zh unknown
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4289815A (en) * | 1978-06-26 | 1981-09-15 | Airwick Industries, Inc. | Cold water-insoluble polyvinyl alcohol pouch for the controlled release of active ingredients |
| WO2016060097A1 (ja) * | 2014-10-16 | 2016-04-21 | 日本合成化学工業株式会社 | ポリビニルアルコール系フィルムおよびその製造方法、並びに偏光フィルム、偏光板 |
| WO2017033552A1 (ja) * | 2015-08-26 | 2017-03-02 | 日本合成化学工業株式会社 | 偏光膜製造用ポリビニルアルコール系樹脂、およびその製造方法、ポリビニルアルコール系フィルムおよびその製造方法、偏光膜、ポリビニルアルコール系樹脂 |
| JP2018010281A (ja) * | 2016-06-29 | 2018-01-18 | 日本合成化学工業株式会社 | ポリビニルアルコール系フィルム、およびその製造方法、ならびに偏光膜 |
| WO2022138720A1 (ja) * | 2020-12-23 | 2022-06-30 | 三菱ケミカル株式会社 | 偏光膜製造用ポリビニルアルコール系フィルム、偏光膜製造用ポリビニルアルコール系フィルムの製造方法、偏光膜 |
| WO2022202861A1 (ja) * | 2021-03-24 | 2022-09-29 | 三菱ケミカル株式会社 | ポリビニルアルコール系フィルム、およびその製造方法、ならびにそれを用いた偏光膜、偏光板 |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2024169407A (ja) * | 2023-05-24 | 2024-12-05 | 長春石油化學股▲分▼有限公司 | ポリビニルアルコールフィルム及びこれから製造された光学フィルム |
Also Published As
| Publication number | Publication date |
|---|---|
| KR20250124293A (ko) | 2025-08-19 |
| CN119866460A (zh) | 2025-04-22 |
| TW202438581A (zh) | 2024-10-01 |
| JPWO2024143239A1 (ja) | 2024-07-04 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109416424B (zh) | 偏光膜用聚乙烯醇系薄膜和其制造方法、以及使用该偏光膜用聚乙烯醇系薄膜的偏光膜 | |
| JP6883990B2 (ja) | ポリビニルアルコール系フィルム、ポリビニルアルコール系フィルムの製造方法、及び偏光膜 | |
| CN116368410B (zh) | 偏光膜制造用聚乙烯醇系薄膜、偏光膜制造用聚乙烯醇系薄膜的制造方法、偏光膜 | |
| JP6953804B2 (ja) | ポリビニルアルコール系フィルム、およびその製造方法、ならびに偏光膜 | |
| WO2017204271A1 (ja) | ポリビニルアルコール系フィルム、およびその製造方法、ならびにそのポリビニルアルコール系フィルムを用いた偏光膜 | |
| TW202248309A (zh) | 聚乙烯醇系薄膜、及其製造方法、以及使用其之偏光膜、偏光板 | |
| JP2022100289A (ja) | 偏光膜製造用ポリビニルアルコール系フィルム、偏光膜製造用ポリビニルアルコール系フィルムの製造方法、偏光膜 | |
| JPWO2017217346A1 (ja) | ポリビニルアルコール系フィルム、およびその製造方法、ならびにそのポリビニルアルコール系フィルムを用いた偏光膜 | |
| KR20250124293A (ko) | 편광막 제조용 폴리비닐 알코올계 필름 및 이의 제조 방법, 및 이를 이용하여 이루어진 편광막 | |
| JP7412081B2 (ja) | 偏光膜製造用ポリビニルアルコール系フィルム、及びそれを用いて得られる偏光膜、ならびにポリビニルアルコール系樹脂水溶液 | |
| JP2021002061A (ja) | ポリビニルアルコール系フィルム、及び偏光膜 | |
| JP7192198B2 (ja) | 偏光膜用ポリビニルアルコール系フィルム、およびその製造方法、ならびに偏光膜、およびその製造方法 | |
| JP6740857B2 (ja) | 偏光膜製造用ポリビニルアルコール系フィルムの製造方法 | |
| WO2024181331A1 (ja) | ポリビニルアルコール系フィルム、偏光膜 | |
| WO2025115240A1 (ja) | ポリビニルアルコール系フィルム、偏光膜 | |
| JP2022100290A (ja) | 偏光膜製造用ポリビニルアルコール系フィルム、偏光膜製造用ポリビニルアルコール系フィルムの製造方法、偏光膜 | |
| WO2025063184A1 (ja) | ポリビニルアルコールフィルム、およびそれを用いた偏光膜、ならびに偏光板、ポリビニルアルコールフィルムの製造方法 | |
| CN118660928A (zh) | 聚乙烯醇系薄膜、和使用了其的偏光膜以及偏光板 | |
| WO2026048839A1 (ja) | ポリビニルアルコール系フィルム、およびそれを用いた偏光膜、ならびに偏光板 | |
| WO2025205953A1 (ja) | ポリビニルアルコール系フィルム、偏光膜、及び偏光板 | |
| TW202400694A (zh) | 聚乙烯醇系薄膜及使用其之偏光膜、以及偏光板 | |
| JP2022148527A (ja) | ポリビニルアルコール系偏光子、偏光板およびその製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 23912019 Country of ref document: EP Kind code of ref document: A1 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202380065464.8 Country of ref document: CN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2024567771 Country of ref document: JP |
|
| WWP | Wipo information: published in national office |
Ref document number: 202380065464.8 Country of ref document: CN |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWP | Wipo information: published in national office |
Ref document number: 1020257008254 Country of ref document: KR |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 23912019 Country of ref document: EP Kind code of ref document: A1 |