EP3559301B1 - Düsenaufbau für das thermische spritzen mittels einer suspension oder einer präcursorlösung - Google Patents
Düsenaufbau für das thermische spritzen mittels einer suspension oder einer präcursorlösung Download PDFInfo
- Publication number
- EP3559301B1 EP3559301B1 EP17826490.9A EP17826490A EP3559301B1 EP 3559301 B1 EP3559301 B1 EP 3559301B1 EP 17826490 A EP17826490 A EP 17826490A EP 3559301 B1 EP3559301 B1 EP 3559301B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- nozzle
- flange
- holder
- tubular element
- suspension
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B7/00—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas
- B05B7/16—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed
- B05B7/20—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed by flame or combustion
- B05B7/201—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed by flame or combustion downstream of the nozzle
- B05B7/205—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed by flame or combustion downstream of the nozzle the material to be sprayed being originally a particulate material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B7/00—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas
- B05B7/14—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas designed for spraying particulate materials
- B05B7/1481—Spray pistols or apparatus for discharging particulate material
- B05B7/1486—Spray pistols or apparatus for discharging particulate material for spraying particulate material in dry state
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B7/00—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas
- B05B7/16—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed
- B05B7/22—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed electrically, magnetically or electromagnetically, e.g. by arc
- B05B7/222—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed electrically, magnetically or electromagnetically, e.g. by arc using an arc
- B05B7/226—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed electrically, magnetically or electromagnetically, e.g. by arc using an arc the material being originally a particulate material
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/12—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying
Definitions
- the invention relates to a nozzle structure for thermal spraying by means of a suspension or a precursor solution.
- the suspension which contains particles and with which a layer can be formed on a substrate, is fed into a burner chamber or into the emerging flame / plasma jet.
- the suspension is formed with a liquid and particles.
- the particles used can be metallic and / or ceramic particles, the mean particle size d 50 of which can be in the nano / submicrometer to 5 ⁇ m range.
- a precursor solution can be injected.
- the particles can be heated and accelerated with a gaseous or liquid fuel according to the so-called High Velocity Oxy Fuel Process (HVOF) by oxidizing the fuel.
- HVOF High Velocity Oxy Fuel Process
- the liquid with which the suspension is formed is either evaporated, pyrolyzed or oxidized.
- the suspension In the atmospheric plasma spray process (APS), the suspension is fed into the plasma torch. There the suspension liquid is evaporated and the resulting particles are heated.
- APS atmospheric plasma spray process
- nozzles are used which cause problems in particular with small internal diameters below 500 ⁇ m.
- the axial direction with which the suspension jet emerges from the nozzle bore can also change successively or continuously, so that a “dancing” jet reaches the burner chamber or a plasma torch.
- the nozzle bores are usually produced by drilling during machining or by erosion. In this case, erosion is preferred especially for small internal diameters. In any case, however, the desired and required dimensional accuracy for the inner diameter and the homogeneous cylindrical shape cannot be maintained. Particular problems arise in the area of the inlet and outlet openings of nozzle bores. A ridge can form.
- Exemplary nozzle structure is, for example, off DE 10 89 614 B , DE 10 2009 024111 A1 and FR 1 105 622 A known.
- the feed is to be referred to throughout as the suspension feed.
- the nozzle insert has, with a tubular element arranged in the direction of the burner chamber or perpendicular to the HVOF flame / plasma torch, and an end face arranged opposite the burner chamber, a flange-shaped widening which, when installed, rests against a seat formed in the holder and thereby the contours of the flange-shaped expansion and the seat are complementary are formed with respect to one another, so that the surfaces of the flange-shaped expansion and the seat are in direct contact with one another, so that an end stop and a seal are formed in this area.
- inorganic salts or organometallic compounds dissolved in water or in organic solvents such as ethanol, isopropanol or butanol can be used as a precursor solution.
- the nozzle insert can be inserted from the connection into the holder through a corresponding opening, in particular after the suspension supply, which can be a line or a hose, has been released, and the flange-shaped widening can then be pushed up to the seat. After connecting the suspension feed, the nozzle assembly can be used as intended. It is obvious that a nozzle insert can be exchanged for a new or different nozzle insert. However, due to wear and tear, an exchange can also be carried out if the feed conditions for the suspension are to be changed. A new or different nozzle insert can have a changed inside diameter of the tubular element and / or a changed length of the tubular element.
- the flange-shaped expansion is geometrically designed and dimensioned identically on the nozzle inserts.
- the tubular element and the flange-shaped widening should advantageously be two individual parts that are non-positively, positively and / or cohesively connected to one another.
- the connection can for example have been made by gluing, soldering, welding and / or a press fit.
- Tubular elements can be parts of a tubular semi-finished product cut to the desired length.
- Such semi-finished products can be produced inexpensively with production methods known per se.
- the flange-shaped widening can advantageously be formed from or with a polymer and the tubular element from metal, preferably from passivated stainless steel.
- a flange-shaped widening can be completely removed be formed from a polymer.
- the sealing can be improved by the properties of the polymer.
- the production of a nozzle insert designed in this way as a composite metal-polymer can easily be achieved by simply injecting the flange-shaped expansion onto a tubular element by means of plastic injection molding.
- a conical area can be present on the flange-shaped expansion, which preferably rests against the seat of the holder in the installed state.
- a cylindrical area which is formed inside the holder and in the area of the seat, can fulfill a guiding function for the nozzle insert if its dimensions and geometric design are adapted to the outer contour of the flange-shaped widening outside a conical area.
- the tubular element should have a maximum internal diameter of 0.8 mm, preferably 0.25 mm.
- channels can be formed in the holder or between the holder and the nozzle insert through which a fluid (gaseous or liquid) can flow for cooling.
- a radially circumferential gap can be present between the inner wall of the holder and the outer wall of the tubular element, with which a thermal insulation effect can be achieved.
- this area there can be an annular element in which a bore is formed through which the tubular element can be passed.
- the inner diameter of this bore should be adapted to the outer diameter of the tubular element so that the annular element can fulfill the function of guiding and radial fixing for the tubular element.
- the ring-shaped element should consist of a material with poor thermal conductivity.
- unit prices can be achieved for the nozzle inserts that are below € 1.
- the exchange for another or a worn nozzle insert is quick and easy.
- the tubular elements can be made available with high and constant dimensional accuracy, so that a particular desired geometric design and dimensioning can be maintained.
- the suspension can be heated in the form of very small droplets (spray form) after exiting the tubular element and the liquid evaporated or oxidized and the particles heated and then accelerated in the direction of the surface of the substrate to be coated.
- connection 1 can be a conventional connection with a union nut.
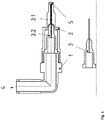
- the connection 1 is provided on a holder 2 which is hollow in its interior.
- a nozzle insert 3 can be inserted from the side of the holder 2 that is open in the area of the connection 1 and inserted up to a seat which is formed in the interior of the holder 2.
- the nozzle insert 3 is formed with a tubular element 3.1 on which a flange-shaped widening 3.2 is formed on the end face pointing in the direction of the inside of the holder.
- the end face of the flange-shaped widening 3.2 pointing in the direction of the outlet opening is conical.
- the seat in the holder 2 has a correspondingly complementary conical area. At least there, the surfaces of the seat and the flange-shaped widening lie flat directly against one another.
- An area adjoining this in the direction of connection 1 can be designed as a hollow cylinder in the holder 2 and as the outer jacket surface of a cylinder on the flange-shaped widening 3.2 of the nozzle insert 3 and form a corresponding longitudinal guide for the nozzle insert 3 in the holder 2.
- the tubular element 3.1 in this example has a length of 9 mm, an inner diameter of 0.25 mm and an outer diameter of 0.52 mm. It was obtained by a cutting process to the desired length from a tubular semi-finished product made of stainless steel.
- the flange-shaped widening 3.2 was formed by means of plastic injection molding in a manner known per se, and there it was at least non-positively and / or cohesively connected to the tubular element 3.1.
- the flange-shaped widening 3.2 can be formed with almost any polymer that can be processed by plastic injection molding.
- the in Figure 1 The example shown is on the end face of the holder 2 an additional inner hollow casing 5, through which the tubular element 3.1 is present in the direction of a burner chamber, not shown, or in the direction of a substrate to be coated by means of thermal spraying.
- the casing 5 can be part of the holder 2 or attached as a separate element to the holder 2, for example by means of a screw connection.
- the casing 5 can in particular fulfill a protective function for the tubular element 3.1.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Electromagnetism (AREA)
- Combustion & Propulsion (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Plasma & Fusion (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Nozzles (AREA)
- Coating By Spraying Or Casting (AREA)
Description
- Die Erfindung betrifft einen Düsenaufbau für das thermische Spritzen mittels einer Suspension oder einer Präkursorlösung. Dabei wird die Suspension, in der Partikel enthalten sind und mit denen auf einem Substrat eine Schicht ausgebildet werden kann, in eine Brennerkammer oder in den austretenden Flamm/Plasmastrahl zugeführt. Die Suspension ist mit einer Flüssigkeit und Partikeln gebildet. Als Partikel können metallische und/oder keramische Partikel eingesetzt werden, deren mittlere Partikelgröße d50 im Bereich nano/submikrometer bis 5.µm liegen kann. Anstatt einer Suspension kann eine Präkursorlösung injiziert werden.
- In der Brennerkammerkönnen die Partikel mit einem gasförmigen oder flüssigen Brennstoff nach dem so genannten High Velocity Oxy Fuel Verfahren (HVOF) durch Oxidation des Brennstoffs erwärmt und beschleunigt werden. Die Flüssigkeit, mit der Suspension gebildet worden ist, wird entweder verdampft, pyrolisiert oder oxidiert.
- Beim atmosphärischen Plasmaspritzen Verfahren (APS) wird die Suspension in die Plasma-Fackel zugeführt. Dort erfolgt die Verdampfung der Suspensionsflüssigkeit und Erwärmung der resultierenden Partikel.
- Für die Zufuhr der Suspension werden Düsen eingesetzt, die insbesondere bei kleinen Innendurchmessern unterhalb 500 µm Probleme bereiten. So kann keine geeignete und insbesondere als Vollstrahl ausgebildete Strahlform eines aus einer Düsenöffnung austretenden Suspensionsstrahls erreicht werden, die auch dauerhaft eingehalten werden kann. Dadurch kann es zu Ablösungen einzelner Tröpfchen, zu einem Zerfall des Strahls kommen.
- Infolge der Art und Weise der Herstellung von Düsenbohrungen durch die die Suspension strömt treten Winkelabweichungen von der gewünschten vorgegebenen Achsrichtung der Strahlbewegungsrichtung auf. Die Achsrichtung mit der der Suspenssionsstrahl aus der Düsenbohrung austritt kann sich auch sukzessive oder stetig ändern, so dass ein "tanzender" Strahl in die Brennerkammer oder in eine Plasma-Fackel gelangt.
- Es kann auch zu einer Reduzierung des Volumenstromes und/oder einer Erhöhung der Geschwindigkeit mit der die Suspension durch die Düsenbohrung strömt und aus dieser Austritt kommen, wenn sich beispielsweise Verunreinigungen in der Düsenbohrung abgesetzt haben oder dort ein Grat ausgebildet worden ist.
- Diese Nachteile treten im Wesentlichen herstellungsbedingt auf. Üblicherweise werden die Düsenbohrungen durch Bohren während einer spanenden Bearbeitung oder durch Erodieren hergestellt. Dabei ist das Erodieren insbesondere bei kleinen Innendurchmessern bevorzugt. In jedem Fall kann jedoch nicht die gewünschte und erforderliche Maßhaltigkeit beim Innendurchmesser und der homogenen Zylinderform eingehalten werden. Besondere Probleme treten dabei im Bereich der Ein- und Austrittsöffnung von Düsenbohrungen auf. Es kann sich ein Grat bilden.
- Besonders nachteilig sind die relativ hohen Kosten für die Fertigung, die bei den üblichen und gewünschten kleinen Innendurchmessern und einem großen Aspektverhältnis (Verhältnis Länge zu Innendurchmesser) erforderlich sind.
- Ablagerungen innerhalb der Düsenbohrung können wenn überhaupt nur sehr aufwändig beseitigt werden.
- Fehler bei der Strahlausbildung beeinflussen das Ergebnis von durch thermisches Spritzen hergestellten Beschichtungen negativ.
- Es ist daher Aufgabe der Erfindung Möglichkeiten für die Zuführung einer Suspension beim thermischen Spritzen anzugeben, mit denen die Qualität verbessert und gleichzeitig die Kosten reduziert sowie die Flexibilität erhöht werden können.
Beispielhafter Düsenaufbau ist z.B. ausDE 10 89 614 B ,DE 10 2009 024111 A1 undFR 1 105 622 A - Erfindungsgemäß wird diese Aufgabe mit einem Düsenaufbau, der die Merkmale des Anspruchs 1 aufweist, gelöst. Vorteilhafte Ausgestaltungen und Weiterbildungen der Erfindung können mit in untergeordneten Ansprüchen bezeichneten Merkmalen realisiert werden.
- Der erfindungsgemäße Düsenaufbau für das thermische Spritzen mittels einer Suspension, in der Partikel enthalten sind, oder einer Präkursorlösung mit denen/der auf einem Substrat eine Schicht ausgebildet wird, und die Suspension in eine Brennerkammer, in eine HVOF-Flame oder in eine Plasma-Fackel in der eine Erwärmung und Beschleunigung der Partikel erreicht wird, zugeführt wird, ist mit einem Anschluss für eine Zuführung für die Suspension oder die Präkursorlösung, einem Halter und einem Düseneinsatz gebildet. Nachfolgend soll die Zuführung durchgängig als Suspensionszuführung bezeichnet werden.
- Der Düseneinsatz weist mit einem in Richtung Brennerkammer oder senkrecht zur HVOF-Flame / Plasma-Fackel angeordneten rohrförmigen Element und einer an der der Brennerkammer gegenüberliegend angeordneten Stirnseite eine flanschförmige Aufweitung auf, die im eingebauten Zustand an einem im Halter ausgebildeten Sitz anliegt und dabei
die Konturen der flanschförmigen Aufweitung und des Sitzes komplementär zueinander ausgebildet sind, so dass die Oberflächen der flänschförmigen Aufweitung und des Sitzes in unmittelbarem Kontakt miteinander stehen, so dass in diesem Bereich ein Endanschlag und eine Abdichtung ausgebildet sind. - Als Präkursorlösung kann man beispielsweise anorganische Salze oder Metallorganische Verbindungen gelöst in Wasser oder in organischen Lösungsmitteln wie z.B. Ethanol, Isopropanol oder Butanol einsetzen.
- Der Düseneinsatz kann, insbesondere nach Lösen der Suspensionszuführung, die eine Leitung oder ein Schlauch sein kann, vom Anschluss in den Halter durch eine entsprechende Öffnung eingesetzt werden und dann die flanschförmige Aufweitung bis an den Sitz heran geschoben werden. Nach dem Anschluss der Suspensionszuführung kann der Düsenaufbau bestimmungsgemäß eingesetzt werden. Es liegt dabei auf der Hand, dass ein Düseneinsatz gegen einen neuen bzw. anderen Düseneinsatz ausgetauscht werden kann. Ein Austausch kann verschleißbedingt aber auch dann durchgeführt werden, wenn die Zuführungsbedingungen der Suspension verändert werden sollen. Dabei kann ein neuer bzw. anderer Düseneinsatz einen veränderten Innendurchmesser des rohrförmigen Elements und/oder eine veränderte Länge des rohrförmigen Elements aufweisen.
- Die flanschförmige Aufweitung ist dabei an den Düseneinsätzen jeweils gleich geometrisch gestaltet und dimensioniert.
- Das rohrförmige Element und die flanschförmige Aufweitung sollten vorteilhaft zwei einzelne Teile sein, die kraft-, form- und/oder stoffschlüssig miteinander verbunden sind. Die Verbindung kann dabei beispielsweise durch Kleben, Löten, Schweißen und/oder eine Presspassung hergestellt worden sein.
- Rohrförmige Elemente können auf die gewünschte Länge geschnittene Teile eines rohrförmigen Halbzeuges sein. Solche Halbzeuge lassen sich kostengünstig mit an sich bekannten Herstellungsverfahren herstellen.
- Die flanschförmige Aufweitung kann vorteilhaft aus oder mit einem Polymer und das rohrförmige Element aus Metall, bevorzugt aus passiviertem Edelstahl gebildet sein. Eine flanschförmige Aufweitung kann dabei vollständig aus einem Polymer gebildet sein. Es besteht aber auch die Möglichkeit, dass lediglich eine mit einem Polymer gebildete Beschichtung im Bereich der flanschförmige Aufweitung vorhanden ist oder ein Verbundmaterial mit einem Polymer dafür eingesetzt wird. Durch die Eigenschaften des Polymers kann die Abdichtung verbessert werden. Außerdem kann die Herstellung eines so ausgebildeten Düseneinsatzes als Verbund Metall - Polymer einfach erreicht werden, indem die flanschförmige Aufweitung einfach durch Kunststoffspritzgießen an ein rohrförmiges Element angespritzt werden kann.
- Vorteilhaft kann an der flanschförmigen Aufweitung ein konischer Bereich vorhanden sein, der bevorzugt im eingebauten Zustand am Sitz des Halters anliegt. Ein zylinderförmiger Bereich, der im Inneren des Halters und im Bereich des Sitzes ausgebildet ist, kann eine Führungsfunktion für den Düseneinsatz erfüllen, wenn dessen Dimensionierung und geometrische Gestaltung an die Außenkontur der flanschförmigen Aufweitung außerhalb eines konisch ausgebildeten Bereichs angepasst ist.
- Das rohrförmige Element sollte einen maximalen Innendurchmesser von 0,8 mm, bevorzugt von 0,25 mm aufweisen.
- Günstig ist es auch, wenn der Halter gekühlt werden kann, dazu können im Halter bzw. zwischen Halter und Düseneinsatz Kanäle ausgebildet sein, durch die ein Fluid (gasförmig oder flüssigförmig) zum Kühlen hindurch strömen kann.
- Zwischen der Innenwand des Halters und der Außenwand des rohrförmigen Elements kann ein radial umlaufender Spalt vorhanden sein, mit dem eine thermische Isolationswirkung erreicht werden kann. In diesem Bereich kann ein ringförmiges Element vorhanden sein, in dem eine Bohrung ausgebildet ist, durch die das rohrförmige Element hindurchgeführt werden kann. Dabei sollte der Innendurchmesser dieser Bohrung an den Außendurchmesser des rohrförmigen Elements angepasst sein, so dass das ringförmige Element die Funktion der Führung und radialen Fixierung für das rohrförmige Element erfüllen kann. Das ringförmige Element sollte dazu aus einem Material mit schlechter thermischer Leitfähigkeit bestehen.
- Mit der Erfindung können für die Düseneinsätze Stückpreise erreicht werden, die unterhalb eines 1 € liegen. Der Austausch gegen einen anderen bzw. einen verschlissenen Düseneinsatz ist einfach und in kurzer Zeit möglich. Insbesondere die rohrförmigen Elemente können mit hoher und konstanter Maßhaltigkeit zur Verfügung gestellt werden, so dass eine jeweils gewünschte geometrische Gestaltung und Dimensionierung eingehalten werden kann.
- Dadurch kann eine sehr gute reproduzierbare und sichere Zuführung einer Suspension in den Prozess des thermischen Spritzens erreicht werden. Lediglich durch entsprechende Gestaltung von Haltern können Düseneinsätze an Brennern (Spritzpistolen) verschiedener Hersteller und für unterschiedlich durchführbare Verfahren des thermischen Spritzens eingesetzt werden.
- Durch geeignete Auswahl eines Düseneinsatzes, was insbesondere den Innendurchmesser des rohrförmigen Elements und sein Länge betrifft können je nach Bedarf verschiedene Zuführungsbedingungen in den Prozess des thermischen Spritzens berücksichtigt werden.
- Es ist auch eine Integration der Zuführung eines Gases zum Zerstäuben der Suspension möglich. Dadurch kann die Suspension nach dem Austritt aus dem rohrförmigen Element in Form sehr kleiner Tröpfchen (Sprayform) erwärmt und dabei die Flüssigkeit verdampft bzw. oxidiert und die Partikel erwärmt und dann in Richtung der zu beschichtenden Oberfläche des Substrates beschleunigt werden.
- Nachfolgend soll die Erfindung anhand eines Beispiels näher erläutert werden.
- Dabei zeigt:
-
Figur 1 eine Schnittdarstellung durch ein Beispiel eines erfindungsgemäßen Düsenaufbaus. - Dabei ist eine Suspensionszuführung 4, von der in
Figur 1 nur ein kleiner Teil angedeutet ist, an einem Anschluss 1 befestigt. Der Anschluss 1 kann eine herkömmliche Verbindung mit einer Überwurfmutter sein. Der Anschluss 1 ist an einem Halter 2 vorhanden, der in seinem Inneren hohl ist. - Nach dem Trennen der Verbindung Anschluss 1 und Suspensionszuführung 4 kann ein Düseneinsatz 3 von der im Bereich des Anschlusses 1 offenen Seite des Halters 2 eingeführt und bis an einen Sitz, der im Inneren des Halters 2 ausgebildet ist, eingeführt werden.
- Der Düseneinsatz 3 ist mit einem rohrförmigen Element 3.1 an dem an der in Richtung des Halterinneren weisenden Stirnseite eine flanschförmige Aufweitung 3.2 ausgebildet ist, gebildet. Die in Richtung Austrittsöffnung weisende Stirnfläche der flanschförmigen Aufweitung 3.2 ist konisch ausgebildet. Der Sitz im Halter 2 weist einen entsprechend komplementär konisch ausgebildeten Bereich auf. Zumindest dort liegen die Oberflächen des Sitzes und der flanschförmigen Aufweitung flächig unmittelbar aneinander. Ein sich daran in Richtung Anschluss 1 anschließender Bereich kann als Hohlzylinder im Halter 2 und als äußere Mantelfläche eines Zylinders an der flanschförmigen Aufweitung 3.2 des Düseneinsatzes 3 ausgebildet sein und eine entsprechende Längsführung für den Düseneinsatz 3 im Halter 2 bilden.
- Das rohrförmige Element 3.1 hat bei diesem Beispiel eine Länge von 9 mm, einen inneren Durchmesser von 0,25 mm und einen Außendurchmesser von 0,52 mm. Es wurde durch ein Trennverfahren auf die gewünschte Länge aus einem rohrförmigen Halbzeug aus Edelstahl erhalten.
- An einer seiner Stirnseiten wurde die flanschförmige Aufweitung 3.2 mittels Kunststoffspritzgießen in an sich bekannter Art und Weise ausgebildet und dort dabei mit dem rohrförmigen Element 3.1 zumindest kraft- und/oder stoffschlüssig verbunden. Die flanschförmige Aufweitung 3.2 kann mit einem nahezu beliebigen durch Kunststoffspritzgießen verarbeitbaren Polymer gebildet werden.
- Bei dem in
Figur 1 gezeigten Beispiel ist an der Stirnseite des Halters 2 eine zusätzliche innen hohle Umkleidung 5, durch die das rohrförmige Element 3.1 in Richtung einer nicht dargestellten Brennerkammer bzw. in Richtung eines mittels thermischen Spritzens zu beschichtenden Substrat vorhanden. Die Umkleidung 5 kann Bestandteil des Halters 2 oder als gesondertes Element am Halter 2, beispielsweise mittels einer Schraubverbindung befestigt sein. Die Umkleidung 5 kann insbesondere eine Schutzfunktion für das rohrförmige Element 3.1 erfüllen.
Claims (7)
- Düsenaufbau für das thermische Spritzen mittels einer Suspension, in der Partikel enthalten sind oder eine Präkursorlösung, mit denen/der auf einem Substrat eine Schicht ausgebildet wird, und die in eine Brennerkammer oder in eine Plasma-Fackel, in der eine Erwärmung und Beschleunigung der Partikel erreicht wird, zugeführt wird, wobei der Düsenaufbau mit einem Anschluss (1) für eine Zuführung (4) für die Suspension oder die Präkursorlösung, einem Halter (2) und einem Düseneinsatz (3) gebildet ist, und
der Düseneinsatz (3) mit einem in Richtung Brennerkammer oder senkrecht zu einer HVOF-Flame oder Plasma-Fackel angeordneten rohrförmigen Element (3.1) und einer an der der Brennerkammer gegenüberliegend angeordneten Stirnseite eine flanschförmige Aufweitung (3.2) aufweist, die im eingebauten Zustand an einem im Halter (2) ausgebildeten Sitz anliegt und dabei
die Konturen der flanschförmigen Aufweitung (3.2) und des Sitzes komplementär zueinander ausgebildet sind, so dass die Oberflächen der flanschförmigen Aufweitung (3.2) und des Sitzes in unmittelbarem Kontakt miteinander stehen, so dass in diesem Bereich ein Endanschlag und eine Abdichtung ausgebildet sind; wobei
die flanschförmige Aufweitung (3.2) aus oder mit einem Polymer und das rohrförmige Element (3.1) aus Metall gebildet ist und
das rohrförmige Element (3.1) und die flanschförmige Aufweitung (3.2) form- und stoffschlüssig mittels Kunststoffspritzgießen miteinander verbunden sind. - Düsenaufbau nach Anspruch 1, dadurch gekennzeichnet, dass das rohrförmige Element (3.1) aus passiviertem korrosionsbeständigem Edelstahl gebildet ist.
- Düsenaufbau nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass am an der flanschförmigen Aufweitung (3.2) ein konischer Bereich vorhanden ist.
- Düsenaufbau nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass der Düseneinsatz (3) austauschbar im Halter (2) befestigt ist.
- Düsenaufbau nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass Düseneinsätze (3) mit unterschiedlicher Länge des rohrförmigen Elements (3.1) und/oder mit unterschiedlichen Innendurchmessern im Halter (2) befestigbar sind.
- Düsenaufbau nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass das rohrförmige Element (3.1) einen maximalen Innendurchmesser von 0,8 mm, bevorzugt von 0,25 mm aufweist.
- Düsenaufbau nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass der Halter (2) kühlbar ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102016125587.4A DE102016125587A1 (de) | 2016-12-23 | 2016-12-23 | Düsenaufbau für das thermische Spritzen mittels einer Suspension oder einer Präcursorlösung |
| PCT/EP2017/083546 WO2018114952A1 (de) | 2016-12-23 | 2017-12-19 | Düsenaufbau für das thermische spritzen mittels einer suspension oder einer präcursorlösung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3559301A1 EP3559301A1 (de) | 2019-10-30 |
| EP3559301B1 true EP3559301B1 (de) | 2021-06-30 |
Family
ID=60953831
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP17826490.9A Active EP3559301B1 (de) | 2016-12-23 | 2017-12-19 | Düsenaufbau für das thermische spritzen mittels einer suspension oder einer präcursorlösung |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US20200290068A1 (de) |
| EP (1) | EP3559301B1 (de) |
| JP (1) | JP2020514534A (de) |
| DE (1) | DE102016125587A1 (de) |
| WO (1) | WO2018114952A1 (de) |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102017130744B4 (de) * | 2017-12-20 | 2022-07-28 | Universität Stuttgart | Vorrichtung und Verfahren zum thermischen Spritzen |
| US12622208B2 (en) | 2023-05-23 | 2026-05-05 | Applied Materials, Inc. | Droplet jet nozzle design |
| CN118374761B (zh) * | 2024-06-21 | 2024-08-30 | 佛山市舒韵五金制品有限公司 | 一种等离子悬浮液喷涂喷嘴 |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1105622A (fr) * | 1954-05-31 | 1955-12-06 | Parker Ste Continentale | Appareil pour la projection de matières plastiques et produits analogues en poudre |
| NL206772A (de) * | 1955-05-02 | 1900-01-01 | ||
| DE8035087U1 (de) * | 1980-12-02 | 1982-09-23 | Sortimat Creuz & Co Gmbh, 7057 Winnenden | Vorrichtung zum herstellen von einmalkanuelen |
| DE10357440B4 (de) * | 2003-02-05 | 2006-02-09 | Hühne, Erwin Dieter | Niedertemperatur-Hochgeschwindigkeits-Flammspritzsystem zum Vorbereiten von Oberflächen und/oder zum thermischen Spritzen von pulverförmigen Spritzzusatzwerkstoffen |
| DE102009024111A1 (de) * | 2009-06-06 | 2010-12-09 | Mtu Aero Engines Gmbh | Düsenhalterung |
| US9089862B2 (en) * | 2010-12-15 | 2015-07-28 | Oerlikon Metco (Us) Inc. | Pressure based liquid feed system for suspension plasma spray coatings |
-
2016
- 2016-12-23 DE DE102016125587.4A patent/DE102016125587A1/de not_active Ceased
-
2017
- 2017-12-19 US US16/473,011 patent/US20200290068A1/en not_active Abandoned
- 2017-12-19 JP JP2019534269A patent/JP2020514534A/ja active Pending
- 2017-12-19 EP EP17826490.9A patent/EP3559301B1/de active Active
- 2017-12-19 WO PCT/EP2017/083546 patent/WO2018114952A1/de not_active Ceased
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2020514534A (ja) | 2020-05-21 |
| DE102016125587A1 (de) | 2018-06-28 |
| EP3559301A1 (de) | 2019-10-30 |
| US20200290068A1 (en) | 2020-09-17 |
| WO2018114952A1 (de) | 2018-06-28 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3204168B1 (de) | Zerstäuberdüse | |
| EP3102335B1 (de) | Kühlvorrichtung für eine spritzdüse bzw. spritzdüsenanordnung mit einer kühlvorrichtung für das thermische spritzen | |
| DE10222660A1 (de) | Verfahren und Vorrichtung zum Hochgeschwindigkeits-Flammspritzen | |
| DE112006002295T5 (de) | Sprühdüsenanordnung zur Atomisierung mittels externer Luftmischung | |
| WO2003041868A2 (de) | Verfahren und vorrichtung zum kaltgasspritzen | |
| EP2941320B1 (de) | Vorrichtung zum thermischen beschichten einer oberfläche | |
| WO2015092008A1 (de) | Vorrichtung und verfahren zum tiegelfreien schmelzen eines materials und zum zerstäuben des geschmolzenen materials zum herstellen von pulver | |
| DE102009005528A1 (de) | Zweistoffdüse | |
| EP2943678B1 (de) | Vorrichtung zum versprayen von flüssigkeit in einen brennraum | |
| WO2021047821A1 (de) | MATERIALABSCHEIDUNGSEINHEIT MIT MEHRFACHER MATERIALFOKUSZONE SOWIE VERFAHREN ZUM AUFTRAGSCHWEIßEN | |
| DE4129120C2 (de) | Verfahren und Vorrichtung zum Beschichten von Substraten mit hochtemperaturbeständigen Kunststoffen und Verwendung des Verfahrens | |
| WO2018114952A1 (de) | Düsenaufbau für das thermische spritzen mittels einer suspension oder einer präcursorlösung | |
| EP2499278A1 (de) | Verfahren und vorrichtung zur bauteilbeschichtung | |
| DE102011107609A1 (de) | Reduktionsmitteleinspritzdüse und Verfahren zur Herstellung einer Reduktionsmitteleinspritzdüse | |
| DE202021104848U1 (de) | Laserspritzpistole, mit der eine Beschichtung mit ultrahoher Bindungsfestigkeit hergestellt werden kann | |
| DE102018129964A1 (de) | Rotationszerstäuber | |
| DE102017130744B4 (de) | Vorrichtung und Verfahren zum thermischen Spritzen | |
| DE102014209171B4 (de) | Verfahren und Vorrichtung zum Fokussieren eines aus einer Ausgabeöffnung einer Ausgabevorrichtung einer Jet-Vorrichtung ausgegebenen viskosen Mediums | |
| DE102013010126B4 (de) | Plasmapulverspritzverfahren und Vorrichtung zur Beschichtung von Paneelen für Kesselwände in Verbindung mit einem Laserstrahlgerät | |
| EP3831498A1 (de) | Bündeldüse zum versprühen eines fluids, anordnung mit einer bündeldüse und verfahren zum herstellen einer bündeldüse | |
| DE102020213695A1 (de) | Bündeldüse zum Versprühen eines Fluids, Anordnung mit einer Bündeldüse und Verfahren zum Herstellen einer Bündeldüse | |
| EP3896190B1 (de) | Verfahren und anlage zur metallischen beschichtung einer bohrungswand | |
| EP4082670B1 (de) | Vorrichtung zum thermischen beschichten mittels drahtlichtbogenspritzen | |
| DE3422904A1 (de) | Duese einer warmspruehpistole fuer kunststoff | |
| EP4260945A1 (de) | Vorrichtung zum thermischen beschichten mittels drahtlichtbogenspritzen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: UNKNOWN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20190722 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17Q | First examination report despatched |
Effective date: 20200625 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20210210 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502017010811 Country of ref document: DE Ref country code: AT Ref legal event code: REF Ref document number: 1406400 Country of ref document: AT Kind code of ref document: T Effective date: 20210715 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210930 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20210630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20211001 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210930 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20211102 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502017010811 Country of ref document: DE |
|
| RAP4 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: FRAUNHOFER-GESELLSCHAFT ZUR FOERDERUNG DER ANGEWANDTEN FORSCHUNG E.V. |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| 26N | No opposition filed |
Effective date: 20220331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20211219 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20211231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211219 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211219 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211219 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211231 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211231 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230524 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20171219 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 1406400 Country of ref document: AT Kind code of ref document: T Effective date: 20221219 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221219 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221219 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210630 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251222 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20260410 Year of fee payment: 5 |