EP2789714B1 - Verarbeitungseinheit mit kondensator und vollautomatisches verarbeitungssystem zur tiefdruckplattenherstellung damit - Google Patents
Verarbeitungseinheit mit kondensator und vollautomatisches verarbeitungssystem zur tiefdruckplattenherstellung damit Download PDFInfo
- Publication number
- EP2789714B1 EP2789714B1 EP12855932.5A EP12855932A EP2789714B1 EP 2789714 B1 EP2789714 B1 EP 2789714B1 EP 12855932 A EP12855932 A EP 12855932A EP 2789714 B1 EP2789714 B1 EP 2789714B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- processing
- condenser
- processing unit
- bath
- making
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D21/00—Processes for servicing or operating cells for electrolytic coating
- C25D21/16—Regeneration of process solutions
- C25D21/18—Regeneration of process solutions of electrolytes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41C—PROCESSES FOR THE MANUFACTURE OR REPRODUCTION OF PRINTING SURFACES
- B41C1/00—Forme preparation
- B41C1/18—Curved printing formes or printing cylinders
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23F—NON-MECHANICAL REMOVAL OF METALLIC MATERIAL FROM SURFACE; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL; MULTI-STEP PROCESSES FOR SURFACE TREATMENT OF METALLIC MATERIAL INVOLVING AT LEAST ONE PROCESS PROVIDED FOR IN CLASS C23 AND AT LEAST ONE PROCESS COVERED BY SUBCLASS C21D OR C22F OR CLASS C25
- C23F1/00—Etching metallic material by chemical means
- C23F1/08—Apparatus, e.g. for photomechanical printing surfaces
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D17/00—Constructional parts, or assemblies thereof, of cells for electrolytic coating
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D21/00—Processes for servicing or operating cells for electrolytic coating
- C25D21/04—Removal of gases or vapours ; Gas or pressure control
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D7/00—Electroplating characterised by the article coated
- C25D7/04—Tubes; Rings; Hollow bodies
Definitions
- the present invention relates to a processing unit including a condenser, which is to be used for a fully automatic gravure plate-making processing system for manufacturing a plate-making roll by performing a series of processes on a plate-making roll to be processed (hereinafter referred to as "unprocessed plate-making roll"), and to a fully automatic gravure plate-making processing system using the processing unit including a condenser.
- US4519887 discloses an apparatus for automatically attaching and detaching cassette-type rolls, which is suited for plating peripheral surfaces of a roll having a shaft, and particularly for plating peripheral surfaces of a photogravure roll, with copper or chromium.
- Current-carrying supporters are exchanged depending upon the type of the roll to be treated, and leak-proof caps are provided, made up of moving caps that slide on the outer side of the spindles and exchange caps that are located between end surfaces of the roll and the moving caps.
- the apparatus can be adapted to different types of rolls having a shaft.
- Patent Document 4 a fully automatic gravure plate-making processing system having high degrees of freedom, which is capable of manufacturing a gravure plate-making roll more quickly as compared to a conventional system, achieving space saving, performing an unattended operation even in the nighttime, flexibly customizing a manufacturing line, and satisfying various customer needs.
- the above-mentioned fully automatic gravure plate-making processing system is configured to manufacture a plate-making roll by performing a series of processes on an unprocessed plate-making roll, and the processes are performed by respective processing units.
- Patent Document 5 A copper plating apparatus described in, for example, Patent Document 5 is known as a further specific example of the conventional processing unit.
- a processing solution vaporized into the form of mist during a plating process is exhausted as it is and filtrated with a filter or the like, and then the resultant is exhausted to the outside.
- the processing solution vaporized into the form of mist during the process is exhausted as it is and filtrated with a filter or the like, and then the resultant is exhausted to the outside. Therefore, every time the plate-making process is performed by each processing unit, the amount of the processing solution is reduced, and as a measure against the reduction in amount of the processing solution, for example, the processing solution is added after the plate-making process by an amount corresponding to the vaporization amount.
- the vapor is particularly liable to be generated, and hence there is a problem in that the vapor is jammed in the middle of the passage even when an exhaust gas cleaning apparatus such as a mist scrubber is mounted.
- the present invention has been made in view of the above-mentioned problems inherent in the conventional technologies, and it is therefore an object thereof to provide a processing unit including a condenser, which is capable of condensing, during a plate-making process to be performed by the processing unit in a fully automatic gravure plate-making processing system, a processing solution vaporized into the form of mist so as to reuse the resultant as the processing solution, and to provide a fully automatic gravure plate-making processing system using the processing unit including a condenser.
- a processing unit including a condenser which is to be used for a fully automatic gravure plate-making processing system for manufacturing a plate-making roll by performing a series of processes on an unprocessed plate-making roll
- the processing unit including: a processing bath; chuck means for holding a gravure cylinder inside the processing bath; an intake port for taking in air, which is provided in a part of the processing bath; an exhaust port for exhausting gas, which is provided in another part of the processing bath, said exhaust port being provided on another side of said processing bath, said intake port facing in a direction of said exhaust port, said intake port, said exhaust port and said processing bath defining a fluid flow path, wherein fluid moves along said fluid flow path from said part of said processing bath to said another part of said processing bath; a condenser provided between the processing bath and the exhaust port; and a processing solution return pipe for returning, to the processing bath, a processing solution obtained by the conden
- the condenser be an air-cooled condenser. This is because space saving can be achieved.
- a mist collector that is a plate having a large number of baffles arranged thereon is taken as an example. This is because, through use of this mist collector, the processing solution vaporized into the form of mist can be collected and liquefied efficiently.
- the present invention is applicable to any processing unit of the type in which the processing solution is used during the plate-making process, and the processing solution is vaporized into the form of mist and then exhausted.
- the processing unit including a condenser be at least one processing apparatus selected from among a copper plating apparatus, a chromium plating apparatus, or an etching apparatus.
- the fully automatic gravure plate-making processing system according to the present invention is constructed by assembling the above-mentioned processing unit including a condenser according to the present invention.
- the present invention has a remarkable effect of providing the processing unit including a condenser, which is capable of condensing, during the plate-making process to be performed by the processing unit in the fully automatic gravure plate-making processing system, the processing solution vaporized into the form of mist so as to reuse the resultant as the processing solution, and providing the fully automatic gravure plate-making processing system using the processing unit including a condenser.
- the processing unit including a condenser As described above, through use of the processing unit including a condenser according to the present invention, during the plate-making process to be performed by the processing unit in the fully automatic gravure plate-making processing system, the processing solution vaporized into the form of mist is condensed so that the resultant can be reused as the processing solution.
- the reduction in amount of the processing solution is suppressed, and hence the cost for the plate-making process is reduced.
- the total amount of gas to be exhausted is reduced, and hence there is an advantage in that the load on the exhaust gas cleaning apparatus such as a filter is reduced and the improvement is satisfactorily achieved in the environmental issues around the system.
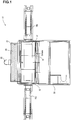
- reference symbol 10 represents a processing unit including a condenser of the present invention.
- the processing unit 10 including a condenser is a processing unit including a condenser, which is to be used for a fully automatic gravure plate-making processing system for manufacturing a plate-making roll by performing a series of processes on an unprocessed plate-making roll.
- the processing unit 10 includes a processing bath 12, chuck means 16a and 16b for holding a gravure cylinder 14 inside the processing bath 12, an intake port 18 for taking in air, which is provided in a part of the processing bath 12, an exhaust port 20 for exhausting gas, which is provided in another part of the processing bath 12, a condenser 22 provided between the processing bath 12 and the exhaust port 20, and a processing solution return pipe 24 for returning, to the processing bath 12, a processing solution obtained by the condenser 22 that liquefies a part of the gas to be exhausted.
- the condenser 22 illustrated in the figures is an air-cooled condenser.
- a mist collector that is a plate (made of hard vinyl chloride) having a large number of baffles 26 arranged thereon is used as the condenser 22. That is, when the processing unit 10 performs a plate-making process (in a case of a copper plating apparatus, a copper plating process) on the gravure cylinder 14, a processing solution vaporized into the form of mist impinges and adheres onto the baffles 26 while passing through the condenser 22. Thus, the mist of the processing solution is collected and condensed into liquid again.
- the processing solution thus liquefied is returned again to the processing bath 12 through the processing solution return pipe 24, and the returned processing solution is reused. Further, a part of the exhaust gas that is not condensed into liquid again is exhausted through the exhaust port 20.
- the processing unit 10 including a condenser in the figures there is described an example in which "SUNLOID” Eliminator manufactured by Sumitomo Bakelite Co., Ltd. is used as the mist collector serving as the condenser 22.
- the mist collector serving as the condenser 22.
- the processing unit 10 including a condenser is used as the processing unit 10 including a condenser.
- the present invention is applicable to any processing unit of the type in which the processing solution is used during the plate-making process, and the processing solution is vaporized into the form of mist and then exhausted.
- the processing unit including a condenser according to the present invention is suitably used as a copper plating apparatus, a chromium plating apparatus, an etching apparatus, or the like.
- reference symbol 28 represents a frame member for supporting components of the processing unit 10, such as an electrode
- reference symbol 30 represents a casing of the processing unit 10.
- the basic structure of the processing unit 10 other than the condenser 22 for example, the structure similar to that of the processing unit described in Patent Document 4 and the like may be employed.
- the fully automatic gravure plate-making processing system according to the present invention is constructed by assembling the processing unit 10 including a condenser according to the present invention into the fully automatic gravure plate-making processing system described in, for example, Patent Documents 1 to 4. Among others, it is suitable to assemble the processing unit including a condenser according to the present invention into the fully automatic gravure plate-making processing system disclosed in Patent Document 4.
- the fully automatic gravure plate-making processing system described in Patent Document 4 is a fully automatic gravure plate-making processing system having high degrees of freedom, which is capable of manufacturing a gravure plate-making roll more quickly as compared to a conventional system, achieving space saving, performing an unattended operation even in the nighttime, flexibly customizing a manufacturing line, and satisfying various customer needs.
- the processing unit including a condenser As described above, through use of the processing unit including a condenser according to the present invention, during the plate-making process to be performed by the processing unit in the fully automatic gravure plate-making processing system, the processing solution vaporized into the form of mist is condensed so that the resultant can be reused as the processing solution.
- the reduction in amount of the processing solution is suppressed, and hence the cost for the plate-making process is reduced.
- the total amount of gas to be exhausted is reduced, and hence there is an advantage in that the load on the exhaust gas cleaning apparatus is reduced and the improvement is satisfactorily achieved in the environmental issues around the system.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Metallurgy (AREA)
- Materials Engineering (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Organic Chemistry (AREA)
- Electrochemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Manufacture Or Reproduction Of Printing Formes (AREA)
- Printing Plates And Materials Therefor (AREA)
- ing And Chemical Polishing (AREA)
Claims (4)
- Bearbeitungseinheit (10), die einen Verdichter (22) umfasst und für ein vollständig automatisiertes Gravur-Plattenherstellungs-Verarbeitungssystem verwendet werden soll, das zur Herstellung einer Plattenherstellungs-Walze durch die Durchführung einer Reihe von Verarbeitungsschritten an einer unbearbeiteten Plattenherstellungs-Walze dient, wobei die Bearbeitungseinheit (10) Folgendes umfasst:ein Bearbeitungsbad (12),ein Spannfutter (16a, 16b) zum Halten eines Gravurzylinders (14) innerhalb des Bearbeitungsbades (12),einen Eingangsanschluss (18) zum Einführen von Luft, der in einem Teil des Bearbeitungsbades (12) vorgesehen ist,einen Entlüftungsanschluss (20) zum Abführen von Gas, der in einem anderen Teil des Bearbeitungsbades vorgesehen ist,wobei der Eingangsanschluss (18) in Richtung des Entlüftungsanschlusses (20) weist und der Eingangsanschluss (18), der Entlüftungsanschluss (20) und das Bearbeitungsbad (12) einen Fluid-Strömungsweg definieren und sich das Fluid längs des Fluid-Strömungsweges von dem erstgenannten Teil des Bearbeitungsbades (12) zu dem besagten anderen Teil des Bearbeitungsbades (12) bewegt,einen Verdichter (22), der zwischen dem Bearbeitungsbad (12) und dem Entlüftungsanschluss (20) vorgesehen ist, undein Bearbeitungslösung-Rückführungsrohr (24), das dazu dient, in das Bearbeitungsbad eine Bearbeitungslösung zurückzuführen, die mithilfe des Verdichters (22) erhalten wird, der einen Teil des abzuführenden Gases verflüssigt,wobei der Verdichter (22) in der Nachbarschaft des Bearbeitungslösung-Rückführungsrohrs (24), des Bearbeitungsbades (12) und des Entlüftungsanschlusses (20) angeordnet ist.
- Bearbeitungseinheit (10), die einen Verdichter (22) umfasst, gemäß Anspruch 1, wobei der Verdichter einen luftgekühlten Verdichter umfasst.
- Bearbeitungseinheit (10), die einen Verdichter (22) umfasst, gemäß Anspruch 1 oder 2, wobei die Bearbeitungseinheit (10), die einen Verdichter (22) umfasst, wenigstens eine Bearbeitungsvorrichtung umfasst, bei der es sich um eine Kupfer-Beschichtungsvorrichtung oder eine Chrom-Beschichtungsvorrichtung und/oder eine Ätzvorrichtung handelt.
- Vollständig automatisiertes Gravurplatten-Herstellungs-Verarbeitungssystem, das durch das Zusammenbauen der Bearbeitungseinheit (10) hergestellt ist, die einen Verdichter (22) gemäß einem der Ansprüche 1 bis 3 umfasst.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2011267471 | 2011-12-07 | ||
| PCT/JP2012/081489 WO2013084929A1 (ja) | 2011-12-07 | 2012-12-05 | 凝縮器付処理ユニット及びそれを用いた全自動グラビア製版処理システム |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP2789714A1 EP2789714A1 (de) | 2014-10-15 |
| EP2789714A4 EP2789714A4 (de) | 2015-09-02 |
| EP2789714B1 true EP2789714B1 (de) | 2018-03-28 |
Family
ID=48574287
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12855932.5A Active EP2789714B1 (de) | 2011-12-07 | 2012-12-05 | Verarbeitungseinheit mit kondensator und vollautomatisches verarbeitungssystem zur tiefdruckplattenherstellung damit |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US20150014154A1 (de) |
| EP (1) | EP2789714B1 (de) |
| JP (1) | JPWO2013084929A1 (de) |
| KR (1) | KR20140019866A (de) |
| CN (1) | CN103732806A (de) |
| ES (1) | ES2666858T3 (de) |
| WO (1) | WO2013084929A1 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20130098875A (ko) * | 2010-10-01 | 2013-09-05 | 가부시키가이샤 씽크. 라보라토리 | 전자동 그라비아 제판용 처리 시스템 |
Family Cites Families (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US10106A (en) * | 1853-10-11 | Improvement in covering metals with gutta-percha and caoutchouc | ||
| US2439491A (en) * | 1942-06-02 | 1948-04-13 | Schiffl Charles | Enclosed electroplating tank |
| US4519887A (en) * | 1983-06-13 | 1985-05-28 | Think Laboratory Co., Ltd. | Apparatus for automatically attaching and detaching cassette-type rolls |
| JPS60179302U (ja) * | 1984-05-07 | 1985-11-28 | 日本電気株式会社 | ウエツト処理装置 |
| US5149411A (en) * | 1991-04-22 | 1992-09-22 | Robert L. Castle | Toxic fumes removal apparatus for plating tank |
| JP3363243B2 (ja) * | 1994-03-16 | 2003-01-08 | 大豊工業株式会社 | めっき工程の蒸気回収装置 |
| JPH09111498A (ja) * | 1995-10-13 | 1997-04-28 | Yazaki Corp | めっき装置 |
| JP2918832B2 (ja) * | 1995-12-15 | 1999-07-12 | 日英ハードクローム工業株式会社 | クロムめっきにおけるクロムめっき液、クロムめっき廃液、クロム酸洗浄水用クローズド・リサイクル・システム |
| US6231728B1 (en) * | 1996-11-22 | 2001-05-15 | Hubert F. Metzger | Electroplating apparatus |
| JP3781388B2 (ja) | 1996-12-28 | 2006-05-31 | 株式会社シンク・ラボラトリー | グラビア製版工場 |
| JPH1121680A (ja) * | 1997-07-01 | 1999-01-26 | Fuji Photo Film Co Ltd | 電子写真刷版のエッチング装置及びエッチング処理方法 |
| DE10051830A1 (de) * | 2000-10-19 | 2002-04-25 | Korrotech Gmbh & Co Kg | Behälter zur Aufnahme eines aggressive Dämpfe abgebenden Mediums |
| JP2005029876A (ja) | 2003-07-11 | 2005-02-03 | Think Laboratory Co Ltd | 硫酸銅メッキ方法 |
| JP4709575B2 (ja) * | 2005-04-15 | 2011-06-22 | 福田金属箔粉工業株式会社 | 銅箔の粗面化処理方法及び粗面化処理液 |
| CN100576578C (zh) * | 2006-04-20 | 2009-12-30 | 无锡尚德太阳能电力有限公司 | 制备太阳电池电极的方法及其电化学沉积装置 |
| JP5004362B2 (ja) | 2006-05-23 | 2012-08-22 | 株式会社シンク・ラボラトリー | グラビア製版ロールの全自動製造システム |
| WO2007135898A1 (ja) | 2006-05-24 | 2007-11-29 | Think Laboratory Co., Ltd. | グラビア製版ロールの全自動製造システム |
| DE102006025847A1 (de) * | 2006-06-02 | 2007-12-06 | Merck Patent Gmbh | Verwendung von Phosphinsäure in der Galvanotechnik |
| JP5757667B2 (ja) | 2010-04-06 | 2015-07-29 | 株式会社シンク・ラボラトリー | 全自動グラビア製版用処理システム |
| CN102425002B (zh) * | 2011-12-29 | 2014-05-28 | 广州杰赛科技股份有限公司 | 采用减压蒸馏技术回用镀银液系统及其回收方法 |
-
2012
- 2012-12-05 EP EP12855932.5A patent/EP2789714B1/de active Active
- 2012-12-05 WO PCT/JP2012/081489 patent/WO2013084929A1/ja not_active Ceased
- 2012-12-05 JP JP2013548262A patent/JPWO2013084929A1/ja active Pending
- 2012-12-05 KR KR1020147000551A patent/KR20140019866A/ko not_active Ceased
- 2012-12-05 CN CN201280038989.4A patent/CN103732806A/zh active Pending
- 2012-12-05 US US14/241,579 patent/US20150014154A1/en not_active Abandoned
- 2012-12-05 ES ES12855932.5T patent/ES2666858T3/es active Active
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2789714A1 (de) | 2014-10-15 |
| WO2013084929A1 (ja) | 2013-06-13 |
| EP2789714A4 (de) | 2015-09-02 |
| KR20140019866A (ko) | 2014-02-17 |
| CN103732806A (zh) | 2014-04-16 |
| US20150014154A1 (en) | 2015-01-15 |
| JPWO2013084929A1 (ja) | 2015-04-27 |
| ES2666858T3 (es) | 2018-05-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US8632955B2 (en) | Conditioning a surface of an aluminium strip | |
| KR20090045197A (ko) | 권취식 진공성막방법 및 권취식 진공성막장치 | |
| JP2011236467A (ja) | エッチング酸廃液処理システム及びエッチング酸廃液処理方法及びこれに適用するエッチング酸廃液処理装置 | |
| EP2789714A1 (de) | Verarbeitungseinheit mit kondensator und vollautomatisches verarbeitungssystem zur tiefdruckplattenherstellung damit | |
| CN105506547A (zh) | 一种光学元件金属化镀膜的纳米掩膜方法 | |
| US7845274B2 (en) | Web-fed printing press | |
| CN212039703U (zh) | 一种工业园区多点位分散式排放有机废气的集中处理装置 | |
| CN218025699U (zh) | 一种剥离液废液处理系统 | |
| JP2002254042A (ja) | 真空排気装置のダスト除去方法及び装置とその操業方法 | |
| US8216654B2 (en) | Components for a film-forming device and method for cleaning the same | |
| CN111533315B (zh) | 表面化学处理制程线线上废水废液零排放循环回用处理工艺 | |
| CN216606674U (zh) | 一种二十辊冷轧机用喷射板 | |
| CN209144251U (zh) | Pvd镀膜基材承载装置 | |
| GB1562589A (en) | Electrotinning process and apparatus | |
| JP4570791B2 (ja) | 連続湿式表面処理における処理液排出量の低減方法 | |
| CN212492334U (zh) | 一种一体化脱硝脱硫系统 | |
| CN222895546U (zh) | 尾气排放处理装置和硼扩散设备 | |
| CN116288275B (zh) | 钛铝沉积机台的工艺腔室暖机方法 | |
| CN218656114U (zh) | 轧辊冷却装置 | |
| CN102381072A (zh) | 平版印刷版用铝支撑体的制造方法及制造装置 | |
| JP2005276523A (ja) | 燃料電池発電システム、および燃料電池評価装置 | |
| CN217139616U (zh) | 一种油雾收集装置的除雾器 | |
| CN208812704U (zh) | 一种减少冷凝滴水的胶印滚筒护板 | |
| JPH078940A (ja) | 廃水処理装置 | |
| CN208756999U (zh) | 一种喷淋塔后端的去水汽装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20140305 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| RA4 | Supplementary search report drawn up and despatched (corrected) |
Effective date: 20150731 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C23F 1/08 20060101ALI20150727BHEP Ipc: B41C 1/18 20060101ALI20150727BHEP Ipc: C25D 21/18 20060101AFI20150727BHEP Ipc: C25D 17/00 20060101ALI20150727BHEP Ipc: B41N 1/06 20060101ALI20150727BHEP Ipc: C25D 7/04 20060101ALI20150727BHEP Ipc: C25D 19/00 20060101ALI20150727BHEP Ipc: C25D 21/04 20060101ALI20150727BHEP |
|
| 17Q | First examination report despatched |
Effective date: 20160224 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20171220 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 983522 Country of ref document: AT Kind code of ref document: T Effective date: 20180415 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602012044597 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2666858 Country of ref document: ES Kind code of ref document: T3 Effective date: 20180508 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180628 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20180328 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180629 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180628 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 983522 Country of ref document: AT Kind code of ref document: T Effective date: 20180328 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180730 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602012044597 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20190103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20181205 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181205 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20181231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181205 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181231 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181205 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181205 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20191203 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180328 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20121205 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180328 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180728 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201205 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251211 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20260130 Year of fee payment: 14 |