EP1851364B1 - Procede de traitement de surface de pieces creuses, cuve de mise en oeuvre d' un tel procede, installation de traitement de surface en continu comprenant une telle cuve - Google Patents
Procede de traitement de surface de pieces creuses, cuve de mise en oeuvre d' un tel procede, installation de traitement de surface en continu comprenant une telle cuve Download PDFInfo
- Publication number
- EP1851364B1 EP1851364B1 EP06709195.9A EP06709195A EP1851364B1 EP 1851364 B1 EP1851364 B1 EP 1851364B1 EP 06709195 A EP06709195 A EP 06709195A EP 1851364 B1 EP1851364 B1 EP 1851364B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- parts
- treatment tank
- tank
- support
- zone
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images



Classifications
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D17/00—Constructional parts, or assemblies thereof, of cells for electrolytic coating
- C25D17/02—Tanks; Installations therefor
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D11/00—Electrolytic coating by surface reaction, i.e. forming conversion layers
- C25D11/005—Apparatus specially adapted for electrolytic conversion coating
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D11/00—Electrolytic coating by surface reaction, i.e. forming conversion layers
- C25D11/02—Anodisation
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D21/00—Processes for servicing or operating cells for electrolytic coating
- C25D21/10—Agitating of electrolytes; Moving of racks
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D7/00—Electroplating characterised by the article coated
- C25D7/04—Tubes; Rings; Hollow bodies
Definitions
- the present invention relates to a method and a tank for surface treatment of metal parts, and more particularly to a conversion treatment such as, for example, an anodizing of an aluminum part. It also relates to a method and a continuous surface treatment plant using such a tank.
- the latter are, for example, degreased and rinsed by dipping in different successive baths.
- the pieces are, for example, soaked in a degreasing bath, then are removed and then soaked in a rinsing bath.
- This correction essentially consists in adapting the treatment according to each load.
- they are manufactured with a rather large volume, which leads to have large tanks and thus leads to produce a large volume of polluting effluents.
- the use of pedals and the consequent dimensions of the process implementation facilities generate maintenance costs also substantial.
- the object of the invention is then to overcome all or part of the disadvantages of existing methods and installation facilities, as mentioned above.
- the present invention provides a process having the features of claim 1, a process vessel having the features of claim 15 and an installation having the features of claim 23.
- the invention thus offers a surface treatment of hollow parts of the conversion treatment type, such as anodization, a process according to which the hollow parts are immersed. completely inside at least one treatment tank containing a liquid characterized in that each hollow part is immersed by making it do at least one rotational movement such that the air bubbles that can be created at the inside of the tank are driven from the inner wall of said hollow part.
- each hollow part is immersed by making it do at least one rotational movement such that the air bubbles that can be created inside the tank are driven from the inner wall of said hollow part.
- a rotational movement of at least 90 ° is made to each hollow part, and preferably 360 °.
- a predetermined number of said hollow parts is placed beforehand on a support comprising at least one holding member adapted to immobilize each of them.
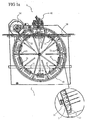
- the figure 1 illustrates a first embodiment given by way of example of a tank (1) intended to implement the treatment method according to the invention.
- the hollow-body treatment tank bearing the general reference (1) comprises a drum (10) rotatably mounted inside the tank, on which each hollow part is able to be fixed.
- the drum (10) comprises, at its outer periphery (100), at least one housing track (11) on which each hollow part is adapted to be fixed.
- the drum (10) comprises fastening means (12), integral with the housing track (11), adapted to fix each support (2) of hollow part (s) by sliding with the support interlocking. (2) in the track (11).
- the support (2) is, in the illustrated embodiment, as described in the application for EP-A-1433,537 .
- the tank (1) comprises its own motor means (13) here an electric type drive motor, which rotates the drum (10).
- the tank (1) also comprises in the embodiment illustrated, its own transmission means (14,15), which transmit the rotational movement of the motor (13) in a rotational movement of the drum (10).
- the drum (10) is notched (15) and meshes with a pinion (14) integral with the shaft (130) motor (13).
- the tank (1) comprises pushing means (4,40) for pushing each support (2) from the outside of the tank to the immersion zone and extraction means (4,41) for extracting each support (2) having been rotated from the exit zone to the outside, the thrust and extraction means being integral with the tank to form an autonomous module.
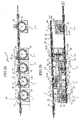
- FIGS. 2a and 2b illustrate an embodiment of a continuous installation for implementing a continuous hollow part surface treatment process.
- an immersion of each support (2) of parts in the tank (1) by making it follow a helical path between the immersion zone (ZI) and the exit zone (ZS) of the tank (1).
- a predetermined number of said hollow parts is placed on a support (2) comprising at least one holding member (21) able to immobilize each of them and in that said support (2) is introduced into the tank (1) so that it comes to push at least one other support (2a) immersed beforehand inside the tank (1), on which is placed another number determined said hollow parts and also comprising at least one holding member (21a) adapted to immobilize each of the parts of the other determined number, to achieve the output of at least one other support (2,2a, 2b ... ) on the second conveying chain (31).
- all the supports (2,2a, 2b ...) are identical and therefore each comprise the same number of holding members (21,21a, 21b ).
- the number of pieces per support (2) may vary according to the unit dimensions of the part (s) to be treated, only the dimensions of each support remains invariable in the described installation.
- At least one rinsing step is carried out by spraying water on at least one of the two conveyor chains (30, 31).
- At least one complementary succeeding tank (1 ', 1 "(7) containing a complementary treatment liquid also having an immersion zone (ZI) and at the same height as the second conveyor chain (31) and in that the supply of each support (2) of the parts exiting the vessel by horizontal thrust from the second conveying chain (31) to the immersion zone is carried out (ZI) of the complementary tank (1 ', 1' ').
- the outlet of each support (2) of the treated parts is preferably produced in the complementary tank (1 ', 1 "(7) by horizontal extraction from an outlet zone (ZS) of the complementary tank ( 1 ', 1 "%) to the first conveying chain (30) conveying in the same direction (SC) for the supply of each support (2) of the parts to the preceding tank (1).
- the continuous surface treatment method of the invention comprises immersing the hollow parts in five different active liquids (LS Satin Liquid, LB Brilliance Liquid, LN Nitric Liquid, Oxidation Fluid).
- LO Clogging Liquid LC in successive steps to achieve the anodisafion of said hollow parts.
- the instaliation according to the invention (3) intended to implement the surface treatment method illustrated, comprises at least one treatment tank (1, 1 ', 1 "(7) capable of containing a treatment liquid (LS, LB, LN, LO, LC) a first conveyor chain (30), arranged at the same height as an immersion zone (ZI) of the vessel (1,1 ', 1 "...) , and able to bring each support (2) of hollow parts at said immersion zone, pushing means (4,40) for horizontally pushing each support (2) of hollow parts from the first conveyor chain (30).
- the thrust means (4,40) preferably comprise at least one hydraulic cylinder (40).
- the extraction means (4,41) preferably comprise at least one hydraulic jack (41).
- the hydraulic jacks (40) and extraction cylinders (41) are identical and a single thrust (40) and a single extraction (41) are arranged opposite one on the other side of the tank (1).
- these thrust cylinders (40) and extraction cylinders (41) are mounted directly on each tank (1,1 ', 1 ", 1"', 1 "” ...) in order to constitute an autonomous module, easily interchangeable since it can be removed individually from the installation, for example in case of momentary failure or change of treatment type.
- the two conveyor chains (30,31) are capable of conveying a plurality of supports (2,2a, 2b, ...) on each of which is placed a predetermined number of said hollow pieces and each comprising at least one holding member (21,21a, 21b, ...) immobilizing each of them.
- the installation (3) comprises at least one rinsing unit (32) by water spraying disposed around at least one of the two conveyor chains (30, 31).
- the tank (1) has, in its upper part, an opening (16) at the edge of which are respectively the immersion zone (ZI) and the exit zone (ZS).
- the installation (3) comprises at least two successive treatment tanks (1,1 ', 1 ", 1' '' ...) and the first (30) and the second (31) conveyor chains are continuous and arranged parallel to one another so that the first chain (30) extends along the immersion zone (ZI) of the upstream vessel (1) and the outlet zone (ZS) of the downstream vessel (1 ', 1 ", 1' '' ...) and that the second chain (31) extends along the outlet zone (ZS) of the vessel upstream (1) and the immersion zone (ZI) of the downstream vessel (1 ', 1 ", 1' '' ).
- each first (30) and second (31) conveyor chain is continuous and straight.
- the plant comprises five successive tanks (1, 1 ', 1 ", 1"', 1 ""), one of which downstream (1 "") is a finishing tank of parts and the other four upstream (1,1 ', 1 ", 1"') are preparation tanks and parts processing.
- the tanks (1,1 ', 1 ", 1''',1”'') are, in the illustrated embodiment, all of different dimensions, in order to have the immersion time necessary for the treatment of the parts in the active liquid used as a treatment liquid (LS, LB, LN, LO, LC)
- the tank (1 "') is an oxidation tank and differs essentially from the others (1,1', 1 ", 1"") in that the current passage between the electrodes and the process to achieve a layer of alumina of desired thickness and quality.It is obvious that the tanks (1,1 ', 1 ", 1"', 1 "") can all be of the same size and, if the case identical.
- the same support (2,2a, 2b, ... 2x 7) therefore follows the identical conveying direction (SC) for each chain (30,31) and therefore alternately passes from a chain (30) to the other (31) after immersion in one of the tanks (1,1 ', 1 ", 1'", 1 "'' ').
- the continuous process according to the invention advantageously makes it possible to eliminate all the existing spreaders in existing processes and consequently all the disadvantages (need to provide support structures for complex lifting beams, reduction of maintenance operations, etc.) and associated risks (numerous displacements and therefore risks of accidents).
- the continuous process according to the invention makes it possible to reduce the number of tanks required and thus to reduce the size of the treatment line. It also allows better control of water and liquid consumption as well as the effluents resulting from the treatment and thus allows an improvement of the pollution control conditions.
- the volume of the necessary liquids is reduced and therefore results in a significant saving, in particular, of active products.
- spray treatments are more reliable because the spraying time of each treatment liquid can be perfectly controlled and reproduced by controlled solenoid valves.
- drum may be provided to rotate the hollow pieces in the vessel as claimed.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Chemical Treatment Of Metals (AREA)
- Coating Apparatus (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
- Treatments Of Macromolecular Shaped Articles (AREA)
- Cleaning By Liquid Or Steam (AREA)
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL06709195T PL1851364T3 (pl) | 2005-02-09 | 2006-01-26 | Sposób obróbki powierzchniowej wydrążonych części, zbiornik do przeprowadzania sposobu tego rodzaju, instalacja do ciągłej obróbki powierzchniowej zawierająca taki zbiornik |
| SI200631806T SI1851364T1 (sl) | 2005-02-09 | 2006-01-26 | Postopek za obdelavo površin votlih delov, posoda za izvajanje tega tipa postopka, naprava za neprekinjeno obdelavo površin, ki vsebuje tako posodo |
| CY20141100548T CY1115346T1 (el) | 2005-02-09 | 2014-07-22 | Μεθοδος για την επεξεργασια της επιφανειας κοιλων τεμαχιων, δεξαμενη για τη διεξαγωγη μιας τετοιας μεθοδου, εγκατασταση για τη συνεχη επεξεργασια επιφανειας η οποια περιλαμβανει μια τετοια δεξαμενη |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR0501323A FR2883576B1 (fr) | 2005-02-09 | 2005-02-09 | Procede de traitement de surface de pieces creuses, cuve de mise en oeuvre d'un tel procede, procede et installation de traitement de surface en continu utilisant une telle cuve |
| PCT/FR2006/000199 WO2006084973A1 (fr) | 2005-02-09 | 2006-01-26 | Procede de traitement de surface de pieces creuses, cuve de mise en oeuvre d' un tel procede, installation de traitement de surface en continu comprenant une telle cuve |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1851364A1 EP1851364A1 (fr) | 2007-11-07 |
| EP1851364B1 true EP1851364B1 (fr) | 2014-04-23 |
Family
ID=35107089
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP06709195.9A Expired - Lifetime EP1851364B1 (fr) | 2005-02-09 | 2006-01-26 | Procede de traitement de surface de pieces creuses, cuve de mise en oeuvre d' un tel procede, installation de traitement de surface en continu comprenant une telle cuve |
Country Status (17)
| Country | Link |
|---|---|
| US (2) | US8293077B2 (OSRAM) |
| EP (1) | EP1851364B1 (OSRAM) |
| JP (1) | JP4982634B2 (OSRAM) |
| KR (2) | KR20070102600A (OSRAM) |
| CN (1) | CN101115869B (OSRAM) |
| BR (1) | BRPI0606879A2 (OSRAM) |
| CA (1) | CA2595511C (OSRAM) |
| CY (1) | CY1115346T1 (OSRAM) |
| DK (1) | DK1851364T3 (OSRAM) |
| ES (1) | ES2483965T3 (OSRAM) |
| FR (1) | FR2883576B1 (OSRAM) |
| MX (1) | MX2007009595A (OSRAM) |
| PL (1) | PL1851364T3 (OSRAM) |
| PT (1) | PT1851364E (OSRAM) |
| RU (1) | RU2409706C2 (OSRAM) |
| SI (1) | SI1851364T1 (OSRAM) |
| WO (1) | WO2006084973A1 (OSRAM) |
Families Citing this family (24)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2900162B1 (fr) * | 2006-04-21 | 2008-08-01 | Frederic Vacheron | Installation de traitement de surface de pieces metalliques, notamment par electrolyse. |
| FR2906265B1 (fr) * | 2006-09-22 | 2008-12-19 | Frederic Vacheron | Installation de traitement de surface de pieces par immerssion dans un liquide de traitement. |
| KR100892995B1 (ko) * | 2008-10-20 | 2009-04-10 | 손치호 | 금속의 아노다이징 처리 방법 및 그 시스템 |
| EP2246460A1 (fr) * | 2009-04-28 | 2010-11-03 | Golden Eagle Trading Ltd | Installation de traitement de surface de pièces |
| ITPR20100047A1 (it) * | 2010-05-21 | 2011-11-22 | Massimiliano Gazzani | Metodo e impianto per l'anodizzazione di un profilato in alluminio o sue leghe |
| JP5613499B2 (ja) * | 2010-08-25 | 2014-10-22 | アルメックスPe株式会社 | 表面処理装置 |
| US11298251B2 (en) | 2010-11-17 | 2022-04-12 | Abbott Cardiovascular Systems, Inc. | Radiopaque intraluminal stents comprising cobalt-based alloys with primarily single-phase supersaturated tungsten content |
| US9724494B2 (en) | 2011-06-29 | 2017-08-08 | Abbott Cardiovascular Systems, Inc. | Guide wire device including a solderable linear elastic nickel-titanium distal end section and methods of preparation therefor |
| EP2684986B1 (de) | 2012-07-12 | 2016-11-02 | Thomas GmbH | Verfahren zum Eloxieren von Flächen an metallischen Hohlkörpern |
| US9045843B2 (en) | 2012-09-14 | 2015-06-02 | Abbott Cardiovascular Systems, Inc. | Electropolishing fixture with lever arm |
| US9145619B2 (en) | 2012-09-14 | 2015-09-29 | Abbott Cardiovascular Systems, Inc. | Electropolishing method including multi-finger contacts |
| US8815061B2 (en) | 2012-09-14 | 2014-08-26 | Abbott Cardiovascular Systems, Inc. | Electropolishing fixture with plunger mechanism |
| US9133563B2 (en) | 2012-09-14 | 2015-09-15 | Abbott Cardiovascular Systems, Inc. | Electropolishing device and method |
| EP2733238A1 (fr) | 2012-11-16 | 2014-05-21 | Cyklos SA | Procédé de traitement de surface, cuve et machine mettant en oeuvre le procédé |
| CA2905536C (en) | 2013-03-15 | 2023-03-07 | Modumetal, Inc. | Electrodeposited compositions and nanolaminated alloys for articles prepared by additive manufacturing processes |
| CA2905575C (en) | 2013-03-15 | 2022-07-12 | Modumetal, Inc. | A method and apparatus for continuously applying nanolaminate metal coatings |
| WO2016044720A1 (en) | 2014-09-18 | 2016-03-24 | Modumetal, Inc. | A method and apparatus for continuously applying nanolaminate metal coatings |
| BR112017005534A2 (pt) | 2014-09-18 | 2017-12-05 | Modumetal Inc | métodos de preparação de artigos por processos de eletrodeposição e fabricação aditiva |
| EP3509812B1 (en) | 2016-09-09 | 2025-04-09 | Modumetal, Inc. | Manufacturing of molds by deposition of material layers on a workpiece, molds and articles obtained by said process |
| CN109963966B (zh) | 2016-09-14 | 2022-10-11 | 莫杜美拓有限公司 | 用于可靠、高通量、复杂电场生成的系统以及由其生产涂层的方法 |
| CN110114210B (zh) | 2016-11-02 | 2022-03-04 | 莫杜美拓有限公司 | 拓扑优化的高界面填充结构 |
| US11286575B2 (en) * | 2017-04-21 | 2022-03-29 | Modumetal, Inc. | Tubular articles with electrodeposited coatings, and systems and methods for producing the same |
| WO2019210264A1 (en) | 2018-04-27 | 2019-10-31 | Modumetal, Inc. | Apparatuses, systems, and methods for producing a plurality of articles with nanolaminated coatings using rotation |
| US12151049B2 (en) | 2019-10-14 | 2024-11-26 | Abbott Cardiovascular Systems, Inc. | Methods for manufacturing radiopaque intraluminal stents comprising cobalt-based alloys with supersaturated tungsten content |
Family Cites Families (34)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1442514A (en) * | 1922-04-22 | 1923-01-16 | Frank J Bell | Electroplating machine |
| US1997013A (en) * | 1930-11-18 | 1935-04-09 | U S Galvanizing & Plating Equi | Method and apparatus for treating pipes |
| US2316972A (en) * | 1941-03-07 | 1943-04-20 | Corning Glass Works | Coating apparatus |
| GB726180A (en) * | 1952-12-04 | 1955-03-16 | Udylite Res Corp | Improvements in or relating to conveyors |
| US2935989A (en) * | 1957-12-04 | 1960-05-10 | Hanson Van Winkle Munning Co | Processing apparatus |
| DE2119401A1 (de) | 1971-04-21 | 1972-11-02 | Dr. Hesse & Cie, 4800 Bielefeld | Mit einem Linearmotor arbeitende Transportvorrichtung bei galvanotechnischen Anlagen |
| US3849284A (en) * | 1972-09-01 | 1974-11-19 | American Can Co | Apparatus method and valve for electrodepositing a coating on interior surfaces of container bodies |
| US4062752A (en) * | 1976-10-04 | 1977-12-13 | Myron Lester Peterson | Plating mechanism |
| SU761606A1 (ru) | 1978-04-25 | 1980-09-07 | Dmitrij S Batskikh | Устройство для химической обработки полых деталей 1 |
| DE3028635A1 (de) * | 1980-07-29 | 1982-03-04 | Degussa Ag, 6000 Frankfurt | Vorrichtung zum partiellen galvanischen beschichten |
| JPS57204091A (en) | 1981-06-10 | 1982-12-14 | Matsushita Electric Industrial Co Ltd | Two-dimensional position information display system |
| CH653374A5 (en) * | 1982-09-30 | 1985-12-31 | Ffa Flug & Fahrzeugwerke Ag | Process and installation for treating aluminium surfaces |
| DE3304940A1 (de) * | 1983-02-12 | 1984-08-16 | Herberts Gmbh, 5600 Wuppertal | Verfahren zum beschichten einseitig offener hohlkoerper |
| US4581260A (en) | 1984-09-25 | 1986-04-08 | Ampex Corporation | Electroless plating method and apparatus |
| JPS6272175A (ja) | 1985-09-26 | 1987-04-02 | Matsushita Electric Ind Co Ltd | 半導体装置の製造方法 |
| JPS63310998A (ja) | 1987-06-13 | 1988-12-19 | Chuo Seisakusho:Kk | バレルメッキ装置 |
| JPH0342045Y2 (OSRAM) | 1987-11-16 | 1991-09-03 | ||
| US4908153A (en) * | 1988-05-06 | 1990-03-13 | Service Tool Die & Mfg. Company | Transport apparatus for electrocoating machines |
| SU1601209A1 (ru) | 1989-01-02 | 1990-10-23 | Львовское Производственное Объединение "Искра" | Устройство дл обработки мелких деталей |
| JPH02305999A (ja) | 1989-05-18 | 1990-12-19 | Fuji Plant Kogyo Kk | 板状被メッキ物の全面メッキ方法、全面メッキ用被メッキ物保持ドラム、全面メッキ装置、および全面メッキ用補助処理装置 |
| JPH05195290A (ja) | 1992-01-23 | 1993-08-03 | Fuji Photo Film Co Ltd | 電解処理装置 |
| DE19641048C2 (de) | 1996-10-04 | 2000-07-20 | Flaekt Ab | Verfahren zum Ein- und Ausbringen von Werkstücken, insbesondere Fahrzeugkarosserien, Vorrichtung und Anlage zur Oberflächenbehandlung von Werkstücken im Durchlauf |
| AT2361U1 (de) | 1997-08-13 | 1998-09-25 | Blau Automobiltechnik Gmbh | Vorrichtung zum galvanisieren von schöpfenden teilen |
| KR100326394B1 (ko) | 1999-03-27 | 2002-03-12 | 이희평 | 니켈-크롬 도금설비 및 도금방법 |
| JP4497437B2 (ja) | 2000-01-14 | 2010-07-07 | 本田技研工業株式会社 | ディッピング処理装置 |
| JP4342671B2 (ja) | 2000-01-19 | 2009-10-14 | 本田技研工業株式会社 | 搬送装置 |
| DE10047968A1 (de) | 2000-09-27 | 2002-04-18 | Flaekt Ab | Vorrichtung und Verfahren zur Oberflächenbehandlung von Werkstücken |
| CN2532089Y (zh) * | 2002-03-22 | 2003-01-22 | 亚硕企业股份有限公司 | 改良的连续电镀槽结构 |
| FR2848881B1 (fr) | 2002-12-24 | 2005-02-25 | Frederic Vacheron | Dispositif support pour pieces creuses et procede de mise en oeuvre d'un tel dispositif |
| JP2004211116A (ja) | 2002-12-27 | 2004-07-29 | Kuroda Seiki Seisakusho:Kk | アルミニウムまたはアルミニウム合金の陽極酸化処理装置 |
| JP4711706B2 (ja) | 2005-03-18 | 2011-06-29 | 三菱電機株式会社 | 空気調和装置 |
| FR2900162B1 (fr) * | 2006-04-21 | 2008-08-01 | Frederic Vacheron | Installation de traitement de surface de pieces metalliques, notamment par electrolyse. |
| FR2900161A1 (fr) | 2006-04-21 | 2007-10-26 | Frederic Vacheron | Installation de traitement de pieces, notamment par electrolyse |
| FR2906265B1 (fr) * | 2006-09-22 | 2008-12-19 | Frederic Vacheron | Installation de traitement de surface de pieces par immerssion dans un liquide de traitement. |
-
2005
- 2005-02-09 FR FR0501323A patent/FR2883576B1/fr not_active Expired - Fee Related
-
2006
- 2006-01-26 PL PL06709195T patent/PL1851364T3/pl unknown
- 2006-01-26 RU RU2007133607/02A patent/RU2409706C2/ru not_active IP Right Cessation
- 2006-01-26 DK DK06709195.9T patent/DK1851364T3/da active
- 2006-01-26 BR BRPI0606879-0A patent/BRPI0606879A2/pt not_active Application Discontinuation
- 2006-01-26 SI SI200631806T patent/SI1851364T1/sl unknown
- 2006-01-26 JP JP2007554590A patent/JP4982634B2/ja not_active Expired - Fee Related
- 2006-01-26 MX MX2007009595A patent/MX2007009595A/es active IP Right Grant
- 2006-01-26 KR KR1020077020320A patent/KR20070102600A/ko not_active Ceased
- 2006-01-26 CA CA2595511A patent/CA2595511C/fr not_active Expired - Fee Related
- 2006-01-26 EP EP06709195.9A patent/EP1851364B1/fr not_active Expired - Lifetime
- 2006-01-26 US US11/883,983 patent/US8293077B2/en not_active Expired - Fee Related
- 2006-01-26 CN CN2006800044412A patent/CN101115869B/zh not_active Expired - Fee Related
- 2006-01-26 ES ES06709195.9T patent/ES2483965T3/es not_active Expired - Lifetime
- 2006-01-26 PT PT67091959T patent/PT1851364E/pt unknown
- 2006-01-26 WO PCT/FR2006/000199 patent/WO2006084973A1/fr not_active Ceased
- 2006-01-26 KR KR1020127015680A patent/KR101251067B1/ko not_active Expired - Fee Related
-
2012
- 2012-04-18 US US13/450,081 patent/US20120199489A1/en not_active Abandoned
-
2014
- 2014-07-22 CY CY20141100548T patent/CY1115346T1/el unknown
Also Published As
| Publication number | Publication date |
|---|---|
| US20080257717A1 (en) | 2008-10-23 |
| JP2008530359A (ja) | 2008-08-07 |
| CN101115869A (zh) | 2008-01-30 |
| SI1851364T1 (sl) | 2014-09-30 |
| RU2007133607A (ru) | 2009-03-20 |
| MX2007009595A (es) | 2007-09-12 |
| ES2483965T3 (es) | 2014-08-08 |
| WO2006084973A1 (fr) | 2006-08-17 |
| KR20070102600A (ko) | 2007-10-18 |
| BRPI0606879A2 (pt) | 2009-12-22 |
| CA2595511A1 (fr) | 2006-08-17 |
| CY1115346T1 (el) | 2017-01-04 |
| DK1851364T3 (da) | 2014-07-28 |
| KR101251067B1 (ko) | 2013-04-05 |
| EP1851364A1 (fr) | 2007-11-07 |
| JP4982634B2 (ja) | 2012-07-25 |
| US20120199489A1 (en) | 2012-08-09 |
| US8293077B2 (en) | 2012-10-23 |
| CA2595511C (fr) | 2010-09-21 |
| FR2883576B1 (fr) | 2009-05-29 |
| CN101115869B (zh) | 2011-05-04 |
| PL1851364T3 (pl) | 2014-09-30 |
| FR2883576A1 (fr) | 2006-09-29 |
| PT1851364E (pt) | 2014-07-28 |
| RU2409706C2 (ru) | 2011-01-20 |
| KR20120084797A (ko) | 2012-07-30 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2595511C (fr) | Procede de traitement de surface de pieces creuses, cuve de mise en oeuvre d' un tel procede, installation de traitement de surface en continu comprenant une telle cuve | |
| EP2064373B1 (fr) | Installation de traitement de surface de pieces par immersion dans un liquide de traitement | |
| CA2759223A1 (fr) | Installation de traitement de surface de pieces | |
| CN115287667A (zh) | 船舶五金配件用防锈装置 | |
| EP1598447B1 (fr) | Procédé de décapage d'une pièce creuse de révolution et dispositif mettant en oeuvre un tel procédé | |
| EP2013383B1 (fr) | Installation de traitement de surface de pieces metalliques, notamment par electrolyse | |
| EP2994411B1 (fr) | Machine pour laver des plumes equipee d'un cylindre de lavage a chambres multiples | |
| FR2887477A1 (fr) | Dispositif de chargement destine au traitement de surface de pieces creuses et bouchees | |
| EP0664162B1 (fr) | Dispositif de traitement des pièces de formes spéciales | |
| FR2900161A1 (fr) | Installation de traitement de pieces, notamment par electrolyse | |
| JP2003147597A (ja) | 節水式水洗装置 | |
| US20020071917A1 (en) | Process and device for treating articles in a dip bath | |
| FR3141188A1 (fr) | Installation pour le rincage de pieces et procede associe | |
| FR2935147A1 (fr) | Dispositif et procede pour l'application d'un revetement sur une piece par electro deposition. | |
| EP2769773A1 (fr) | Installation de traitement de surface de pièces par immersion | |
| FR2711146A1 (fr) | Installation et procédé de traitement en continu des peaux ou cuirs dans un liquide. | |
| BE1019582A5 (fr) | Dispositif et procede pour le traitement et le tannage de peaux et procede associe. | |
| FR2711144A1 (fr) | Procédé et installation de reverdissage en continu des peaux ou cuirs dans un liquide. | |
| FR3026111A1 (fr) | Systeme d'evacuation pour le controle macrographique d'une piece creuse | |
| EP2733238A1 (fr) | Procédé de traitement de surface, cuve et machine mettant en oeuvre le procédé | |
| FR2681336A1 (fr) | Installation pour effectuer un depot electrolytique, en particulier sur les parois internes d'un bloc-cylindres de moteur a combustion interne de vehicule automobile. | |
| FR2958301A1 (fr) | Procede et installation pour traiter la surface de pieces, par voie liquide. | |
| FR2750437A1 (fr) | Procede et installation de revetement electrolytique par une couche metallique de la surface d'un cylindre pour coulee continue de bandes metalliques minces |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20070724 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: VACHERON, FREDERIC |
|
| 17Q | First examination report despatched |
Effective date: 20100721 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: TORNOS MANAGEMENT HOLDING SA |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20131203 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 663944 Country of ref document: AT Kind code of ref document: T Effective date: 20140515 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: FRENCH |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602006041184 Country of ref document: DE Effective date: 20140605 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: BUGNION S.A., CH |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 Effective date: 20140724 Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20140721 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2483965 Country of ref document: ES Kind code of ref document: T3 Effective date: 20140808 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: T3 Ref document number: E 16783 Country of ref document: SK |
|
| REG | Reference to a national code |
Ref country code: EE Ref legal event code: FG4A Ref document number: E009561 Country of ref document: EE Effective date: 20140723 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20140401431 Country of ref document: GR Effective date: 20140901 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602006041184 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E021500 Country of ref document: HU |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20150126 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602006041184 Country of ref document: DE Effective date: 20150126 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20170119 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LT Payment date: 20170120 Year of fee payment: 12 Ref country code: FR Payment date: 20170120 Year of fee payment: 12 Ref country code: SE Payment date: 20170119 Year of fee payment: 12 Ref country code: EE Payment date: 20170119 Year of fee payment: 12 Ref country code: MC Payment date: 20170123 Year of fee payment: 12 Ref country code: CH Payment date: 20170131 Year of fee payment: 12 Ref country code: GR Payment date: 20170124 Year of fee payment: 12 Ref country code: FI Payment date: 20170120 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IS Payment date: 20170119 Year of fee payment: 12 Ref country code: CY Payment date: 20170120 Year of fee payment: 12 Ref country code: AT Payment date: 20170123 Year of fee payment: 12 Ref country code: PT Payment date: 20170123 Year of fee payment: 12 Ref country code: GB Payment date: 20170119 Year of fee payment: 12 Ref country code: LV Payment date: 20170120 Year of fee payment: 12 Ref country code: LU Payment date: 20170123 Year of fee payment: 12 Ref country code: IE Payment date: 20170123 Year of fee payment: 12 Ref country code: DK Payment date: 20170119 Year of fee payment: 12 Ref country code: BG Payment date: 20170123 Year of fee payment: 12 Ref country code: BE Payment date: 20170119 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20170120 Year of fee payment: 12 Ref country code: ES Payment date: 20170120 Year of fee payment: 12 Ref country code: IT Payment date: 20170124 Year of fee payment: 12 |
|
| REG | Reference to a national code |
Ref country code: EE Ref legal event code: MM4A Ref document number: E009561 Country of ref document: EE Effective date: 20180131 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP Effective date: 20180131 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MM4D Effective date: 20180126 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20180201 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 663944 Country of ref document: AT Kind code of ref document: T Effective date: 20180126 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20180126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180127 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180726 Ref country code: CY Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 Ref country code: LT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180131 Ref country code: EE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180131 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20180928 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20180131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180801 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180131 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180131 Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180802 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180131 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180131 Ref country code: BG Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180806 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20190115 Year of fee payment: 14 Ref country code: RO Payment date: 20190114 Year of fee payment: 14 Ref country code: PL Payment date: 20190110 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: HU Payment date: 20190116 Year of fee payment: 14 Ref country code: SI Payment date: 20190110 Year of fee payment: 14 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180131 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SK Payment date: 20190111 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20190731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180127 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: MM4A Ref document number: E 16783 Country of ref document: SK Effective date: 20200126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200126 Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200126 Ref country code: SK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200127 Ref country code: HU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200127 |
|
| REG | Reference to a national code |
Ref country code: SI Ref legal event code: KO00 Effective date: 20201104 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200126 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20220119 Year of fee payment: 17 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180126 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602006041184 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230801 |