EP1718441B1 - Verfahren zur herstellung und zum schneiden von relativ kleinen elementen - Google Patents
Verfahren zur herstellung und zum schneiden von relativ kleinen elementen Download PDFInfo
- Publication number
- EP1718441B1 EP1718441B1 EP05717624A EP05717624A EP1718441B1 EP 1718441 B1 EP1718441 B1 EP 1718441B1 EP 05717624 A EP05717624 A EP 05717624A EP 05717624 A EP05717624 A EP 05717624A EP 1718441 B1 EP1718441 B1 EP 1718441B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cutting
- sheet
- fact
- cylinders
- relatively small
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F1/00—Perforating; Punching; Cutting-out; Stamping-out; Apparatus therefor
- B26F1/38—Cutting-out; Stamping-out
- B26F1/384—Cutting-out; Stamping-out using rotating drums
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/20—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof characterised by a particular use or purpose
- B42D25/29—Securities; Bank notes
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H21/00—Non-fibrous material added to the pulp, characterised by its function, form or properties; Paper-impregnating or coating material, characterised by its function, form or properties
- D21H21/14—Non-fibrous material added to the pulp, characterised by its function, form or properties; Paper-impregnating or coating material, characterised by its function, form or properties characterised by function or properties in or on the paper
- D21H21/40—Agents facilitating proof of genuineness or preventing fraudulent alteration, e.g. for security paper
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D7/18—Means for removing cut-out material or waste
- B26D7/1845—Means for removing cut-out material or waste by non mechanical means
- B26D7/1863—Means for removing cut-out material or waste by non mechanical means by suction
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H21/00—Non-fibrous material added to the pulp, characterised by its function, form or properties; Paper-impregnating or coating material, characterised by its function, form or properties
- D21H21/14—Non-fibrous material added to the pulp, characterised by its function, form or properties; Paper-impregnating or coating material, characterised by its function, form or properties characterised by function or properties in or on the paper
- D21H21/40—Agents facilitating proof of genuineness or preventing fraudulent alteration, e.g. for security paper
- D21H21/44—Latent security elements, i.e. detectable or becoming apparent only by use of special verification or tampering devices or methods
- D21H21/48—Elements suited for physical verification, e.g. by irradiation
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T83/00—Cutting
- Y10T83/04—Processes
- Y10T83/0524—Plural cutting steps
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T83/00—Cutting
- Y10T83/768—Rotatable disc tool pair or tool and carrier
- Y10T83/7809—Tool pair comprises rotatable tools
- Y10T83/7851—Tool pair comprises disc and cylindrical anvil
Definitions
- the invention relates to a method for manufacturing relatively small format elements such as boards, and in particular the cutting method, and the corresponding devices.
- planchettes for authenticating documents.
- These boards are similar to confetti, usually circular or hexagonal. They can include authentication agents.
- To manufacture security papers or bank note papers containing boards they are introduced into the aqueous dispersion containing cellulose fibers or synthetic fibers and other additives commonly used in the paper industry. When the aqueous suspension is drained on a fabric of a round-form or flat-table paper machine called Fourdrinier, a number of boards are placed on the surface of the sheet of paper thus formed, and then the sheet is dried. .
- the sheet may also be relative to the decorative field, the boards being then for decorative use.
- the sheets are plastic sheets and / or light weight paper.
- overlay sheet usually used as a protective sheet in the field of decorative laminated papers; this sheet is traditionally made by draining an aqueous suspension of slightly refined cellulose fibers, of the order of 20 ° SR (Schoepper-Riegler degrees), and containing a wet strength agent, of low weight, of the order of 25-40 g / m 2 .
- the stamping process being slow and the sheets used thin, about 50 to 100 microns thick, it is generally stamped several stacked sheets, three to four sheets most often.
- a disadvantage is that there is a deformation of the sheets during stamping especially at the level of the bottom sheets, which creates irregular boards. Another disadvantage is that it is difficult to change the shape of punches or pins because they are plates in one piece. Another disadvantage is that there is sufficient space between the punches or pins so that the sheet is well maintained during stamping, resulting in a large sheet waste, especially since the sheet is a sheet expensive because it includes impressions, other security features, and authentication agents. Another disadvantage is that the larger the size of the boards, the more the stamping becomes difficult. The current boards have a limited size of about 1.5 mm. A disadvantage is that their small size does not allow to print texts or patterns clearly visible and / or readable. A disadvantage is therefore that this stamping process does not easily provide boards of larger size.
- the objects of the invention are to solve the disadvantages described above.
- the goals are achieved by proposing a new method of manufacturing relatively small format elements and in particular a new cutting method.
- steps are carried out in line, and preferably at a speed of between 20 and 150 m / min.
- the wound sheet is a sheet of paper, nonwoven, plastic or a complex of these paper / plastic materials, paper / nonwoven, plastic / nonwoven or paper / plastic / nonwoven in one any order.
- the plastic is in particular polyester.
- the sheet is printed by flexography.
- the sheet is printed in a proportion of 1 to 10 g / m 2 per side, preferably between about 2 and 5 g / m 2 per side, in dry weight.
- the sheet is printed on one side.
- the sheet is printed on its two faces successively by recto-verso, in particular by turning the sheet or by inversion of rotation of a printing unit.
- the sheet has a thickness of between about 50 and 110 ⁇ m.
- the detached elements are recovered by dehulling, in particular by peel bar and suction.
- the detached element has its largest dimension of between 0.5 and 6 mm, preferably between 1 and 4 mm.
- the invention also relates to the cutting method per se.
- This method of cutting relatively small format elements is characterized by the fact that, starting from a sheet, these sheets are cut out "in the flesh" in a continuous succession at least two cutting patterns which intersect so as to constitute a resultant pattern which will form a detached element constituting said relatively small-sized element, this cutting taking place by means of a succession of synchronized cutting cylinders respectively carrying a cutting pattern, anvil cylinders being interposed between these cutting cylinders.
- the invention also relates to the cutter full flesh ("bottom").
- This device for cutting relatively small format elements, especially such as boards is characterized by the fact that it comprises a rotary cutting device comprising a succession of synchronized cutting cylinders comprising respective cutting threads, anvil cylinders. being interspersed between these cutting cylinders, the cutting nets on the cylinders complementing so as to form a separate figure when the cutting cylinders rotate synchronously and in a suitable setting. Cutting nets corresponding to cutting patterns that intersect as described above.
- each cutting cylinder is a magnetic cylinder covered with a magnetizable flexible plate retained by the magnetization forces, in particular steel, carrying electrochemically etched cutting threads.
- this cutting device comprises an anvil base cylinder.
- the invention also relates to the device for manufacturing said relatively small format elements, particularly such as boards, which is characterized in that it comprises a reel holder, a printing device with at least one printing unit, a cutting device as described above.
- this manufacturing device comprises a printing device comprising at least two printing units with a set of rollover bar between the groups.
- this manufacturing device comprises a printing device comprising at least two printing units with a device for reversing the rotation of one of the printing units.
- this manufacturing device comprises, after the cutting device, a dehulling device, in particular by peeling bar and suction.
- this manufacturing device comprises a device for treating against static electricity.
- the figure 1 schematically shows a manufacturing device according to the invention.
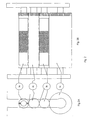
- the figure 2 shows the cylinders of the cutting device according to the invention, the Figure 2A being a side view of said cylinders and the Figure 2B being a front view and detailed.
- FIG. 2B A detail of the cutting cylinders with the cutting patterns is presented on the Figure 2B .
- the patterns intertwine to form a resulting pattern that is a disc (confetti type) that forms a detached element that will constitute a planchette.
- the device of the figure 1 can rotate at a speed of between 20 to 150 m / min.
- the boards are made as follows: the sheet of paper is unwound, the upper surface is printed with fluorescent inks of 3 g / m 2 , to make a pattern representing a flag, the sheet is turned over by flipping and to a registration recto / verso, one prints the other face according to the same motive.
- the print is dried by a UV radiation device. Other hot air or infra-red drying devices could be used.
- the sheet is driven to the cutting device.
- cutting patterns according to the invention which can intersect to form a detachable resulting pattern as well as the resulting pattern are presented on the Figures 3 to 10 of the drawing board in each figure, the first two patterns represent intersecting cutting patterns and the bottom pattern represents the resulting pattern which will correspond to the relatively small size element, for example a safety board.
- the actual dimensions of the elements are given in millimeters in the figure.
Landscapes
- Finance (AREA)
- Forests & Forestry (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Business, Economics & Management (AREA)
- Accounting & Taxation (AREA)
- Life Sciences & Earth Sciences (AREA)
- Printing Methods (AREA)
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
- Polishing Bodies And Polishing Tools (AREA)
- Turning (AREA)
- Absorbent Articles And Supports Therefor (AREA)
- Making Paper Articles (AREA)
Claims (20)
- Verfahren zum Herstellen von Elementen mit verhältnismäßig kleinem Format, insbesondere von Plättchen, das die folgenden Schritte umfasst:- Abwickeln eines aufgewickelten Blatts,- eventuell Bedrucken dieses Blatts wenigstens teilweise auf wenigstens einer Seite, dann- tiefes Ausschneiden "bis zum Boden" des Blatts in einer Folge aus wenigstens zwei Ausschneidemustern, die sich kreuzen, derart, dass ein resultierendes Muster gebildet wird, das ein losgelöstes Element bildet, das das Element mit verhältnismäßig kleinem Format bildet, wobei dieses Ausschneiden mit Hilfe einer Folge von Ausschneidezylindern (3a, 3b) erfolgt, die synchronisiert sind und jeweils eines der Ausschneidemuster tragen, wobei zwischen diese Ausschneidezylinder Ambosszylinder (3c, 3d) eingefügt sind, wobei sich das Blatt zwischen allen diesen Zylindern (3a, 3b, 3c, 3d) bewegt,- Wiedergewinnen der abgelösten Elemente, die die Elemente mit verhältnismäßig kleinem Format bilden.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass alle Schritte in einer Linie erfolgen.
- Verfahren nach Anspruch 2, dadurch gekennzeichnet, dass es mit einer Geschwindigkeit im Bereich von 20 bis 150 m/min ausgeführt wird.
- Verfahren nach einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, dass das Blatt ein Blatt aus Papier, aus Vlies, aus Kunststoff oder aus einem Komplex aus diesen Materialien ist.
- Verfahren nach einem der Ansprüche 1 bis 4, dadurch gekennzeichnet, dass das Blatt durch Flexographie bedruckt wird.
- Verfahren nach einem der Ansprüche 1 bis 5, dadurch gekennzeichnet, dass das Blatt in einer Menge von 1 bis 10 g/m2 pro Seite, vorzugsweise von etwa 2 bis 5 g/m2 pro Seite bedruckt wird.
- Verfahren nach einem der Ansprüche 1 bis 6, dadurch gekennzeichnet, dass das Blatt auf einer einzigen Seite bedruckt wird.
- Verfahren nach einem der Ansprüche 1 bis 6, dadurch gekennzeichnet, dass das Blatt auf seinen beiden Seiten nacheinander durch Festlegen von Vorderseite und Rückseite, insbesondere durch Umdrehen des Blatts oder durch Umkehrung der Drehung einer Druckgruppe (2a, 2b) bedruckt wird.
- Verfahren nach einem der Ansprüche 1 bis 8, dadurch gekennzeichnet, dass das Blatt eine Dicke besitzt, die im Bereich von etwa 50 bis 110 µm liegt.
- Verfahren nach einem der Ansprüche 1 bis 9, dadurch gekennzeichnet, dass die abgelösten Elemente durch Abschälen, insbesondere durch Schälstab und Ansaugen, wiedergewonnen werden.
- Herstellungsverfahren nach einem der Ansprüche 1 bis 10, dadurch gekennzeichnet, dass das abgelöste Element seine größte Abmessung im Bereich von 0,5 bis 6 mm, vorzugsweise von 1 bis 4 mm, hat.
- Verfahren zum Ausschneiden von Elementen mit verhältnismäßig kleinem Format, insbesondere von Plättchen, dadurch gekennzeichnet, dass ausgehend von einem Blatt dieses Blatt ununterbrochen tief "bis zum Boden" in einer Folge aus wenigstens zwei Ausschneidemustern, die sich kreuzen, ausgeschnitten wird, um ein resultierendes Motiv zu bilden, das ein abgelöstes Element bildet, das das Element mit verhältnismäßig kleinem Format bildet, wobei dieses Ausschneiden mit Hilfe einer Folge von Ausschneidezylindern (3a, 3b) erfolgt, die synchronisiert sind und jeweils eines der Ausschneidemuster tragen, wobei zwischen diese Ausschneidezylinder Ambosszylinder (3c, 3d) eingefügt sind.
- Vorrichtung zum Ausschneiden (3) von Elementen mit verhältnismäßig kleinem Format, insbesondere von Plättchen, dadurch gekennzeichnet, dass sie eine rotierende Ausschneidevorrichtung umfasst, die eine Folge von synchronisierten Ausschneidezylindern (3a, 3b) enthält, die jeweilige Ausschneideschraubengänge besitzen, wobei zwischen diese Ausschneidezylinder Ambosszylinder (3c, 3d) eingefügt sind, wobei die Ausschneideschraubengänge an den Zylindern dadurch vervollständigt sind, dass sie eine vollwertige Figur bilden, wenn sich die Ausschneidezylinder auf synchronisierte Weise und mit einer geeigneten Einstellung drehen.
- Ausschneidevorrichtung (3) nach Anspruch 13, dadurch gekennzeichnet, dass jeder Ausschneidezylinder (3a, 3b) ein magnetischer Zylinder ist, der mit einer magnetisiertJaren nachgiebigen Platte, die durch Magnetkräfte gehalten wird, insbesondere aus Stahl, abgedeckt ist, und die Ausschneideschraubengänge trägt, die elektrochemisch graviert sind.
- Ausschneidevorrichtung (3) nach einem der Ansprüche 13 bis 14, dadurch gekennzeichnet, dass sie einen Basis-Ambosszylinder (3e) enthält.
- Vorrichtung zum Herstellen von Elementen mit verhäftnismäf3ig kleinem Format, insbesondere von Plättchen, dadurch gekennzeichnet, dass sie einen Haspelträger (1), eine Druckvorrichtung (2) mit wenigstens einer Druckgruppe (2a, 2b) sowie eine Ausschneidevorrichtung (3) nach den Ansprüchen 13 bis 15 umfasst.
- Vorrichtung nach dem vorhergehenden Anspruch 16, dadurch gekennzeichnet, dass sie eine Druckvorrichtung (2) umfasst, die wenigstens zwei Druckgruppen (2a, 2b) enthält, wobei zwischen den Gruppen eine Anordnung aus Blattumwendestäben (2r) vorhanden ist.
- Vorrichtung nach Anspruch 16, dadurch gekennzeichnet, dass sie eine Druckvorrichtung (2) umfasst, die wenigstens zwei Druckgruppen (2a, 2b) enthält, wobei eine Drehumkehrvorrichtung für eine der Druckgruppen vorhanden ist.
- Herstellungsvorrichtung nach einem der vorhergehenden Ansprüche 16 bis 18, dadurch gekennzeichnet, dass sie hinter der Ausschneidevorrichtung (3) eine Vorrichtung (4) zum Abschälen, insbesondere durch Schälstab und Ansaugen, umfasst.
- Herstellungsvorrichtung nach einem der vorhergehenden Ansprüche 16 bis 19, dadurch gekennzeichnet, dass sie eine Vorrichtung für die Behandlung gegen statische Elektrizität umfasst.
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL05717624T PL1718441T3 (pl) | 2004-02-11 | 2005-02-11 | Sposób produkcji i wykrawania elementów względnie małego formatu |
| SI200530827T SI1718441T1 (sl) | 2004-02-11 | 2005-02-11 | Postopek izdelave in izreza elementov relativno majhnega formata |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR0401329A FR2865957B1 (fr) | 2004-02-11 | 2004-02-11 | Procede de fabrication et de decoupe d'elements de format relativement petit, dispositifs correspondants, elements et feuilles comportant lesdits elements |
| PCT/FR2005/000335 WO2005077622A2 (fr) | 2004-02-11 | 2005-02-11 | Procede de fabrication et de decoupe d’elements de format relativement petit |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1718441A2 EP1718441A2 (de) | 2006-11-08 |
| EP1718441B1 true EP1718441B1 (de) | 2009-08-19 |
Family
ID=34778667
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05717624A Expired - Lifetime EP1718441B1 (de) | 2004-02-11 | 2005-02-11 | Verfahren zur herstellung und zum schneiden von relativ kleinen elementen |
Country Status (11)
| Country | Link |
|---|---|
| US (1) | US20080042425A1 (de) |
| EP (1) | EP1718441B1 (de) |
| AT (1) | ATE439960T1 (de) |
| BR (1) | BRPI0507566A (de) |
| CA (1) | CA2555588A1 (de) |
| DE (1) | DE602005016081D1 (de) |
| ES (1) | ES2332004T3 (de) |
| FR (1) | FR2865957B1 (de) |
| PL (1) | PL1718441T3 (de) |
| SI (1) | SI1718441T1 (de) |
| WO (1) | WO2005077622A2 (de) |
Families Citing this family (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US8287993B2 (en) | 2004-09-15 | 2012-10-16 | Crane & Co., Inc. | Security device and novel anti-counterfeit product employing same |
| DE102005047646B4 (de) * | 2005-09-23 | 2007-08-23 | Heino Ilsemann Gmbh | Vorrichtung zum Ausstanzen von Zuschnitten aus bahnförmigem Material |
| FR2904835B1 (fr) * | 2006-08-08 | 2010-03-19 | Arjowiggins | Elements de securite de format relativement petit comprenant un trou traversant et feuille les comprenant |
| FR2929965B1 (fr) * | 2008-04-11 | 2010-05-21 | Arjowiggins Licensing Sas | Feuille de securite comportant un ruban presentant une zone d'opacite reduite. |
| TWI443612B (zh) * | 2009-04-07 | 2014-07-01 | Sicpa Holding Sa | 受壓變色保密元件 |
| FR2951866B1 (fr) | 2009-10-27 | 2011-11-25 | Arjowiggins Security | Procede de fabrication d'un support integrant un dispositif electronique |
| FR2951867A1 (fr) | 2009-10-27 | 2011-04-29 | Arjowiggins Security | Procede de fabrication d'un support comportant un dispositif electronique |
| FR2995114B1 (fr) | 2012-09-03 | 2015-09-04 | Arjowiggins Security | Procede d'authentification a partir de la teneur en matiere bio-sourcee. |
| KR102077614B1 (ko) | 2017-08-18 | 2020-02-17 | 주식회사 엘지화학 | 복수 패턴 영역을 가지는 모듈의 제조방법, 그 제조방법에 따른 복수 패턴 영역을 가지는 모듈, 및 회절격자모듈 또는 회절격자모듈용 몰드의 제조방법 |
| CN112581637B (zh) * | 2021-01-26 | 2022-08-12 | 重庆旅游云信息科技有限公司 | 一种景区智能防疫信息读取检票设备 |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1806305B2 (de) * | 1968-10-31 | 1971-10-21 | Vorrichtung zum gratlosen abscheren von flachwalzmaterial | |
| DE3706855C3 (de) * | 1987-03-04 | 1993-12-02 | Schleicher Co Feinwerktech | Schneideinrichtung für Vorrichtungen zum Zerkleinern von Dokumenten etc. |
| GB8811671D0 (en) * | 1988-05-17 | 1988-06-22 | Wiggins Teape Group Ltd | Security & decorative paper |
| US5697649A (en) * | 1995-05-11 | 1997-12-16 | Crane & Co., Inc. | Articles employing a magnetic security feature |
| US6350342B1 (en) * | 1996-09-09 | 2002-02-26 | Tamarack Products Inc. | Method of making integrated label products |
| US6022442A (en) * | 1997-07-30 | 2000-02-08 | Mtl Modern Technologies Lizenz Gmbh | Method for making a card product |
| US6138544A (en) * | 1998-04-27 | 2000-10-31 | Newell; Gregory J. | Die-cutter with planetary configuration |
| US6533325B1 (en) * | 2000-06-14 | 2003-03-18 | Tamarack Products, Inc. | Integral card and method of making |
| EP1401637A4 (de) * | 2001-06-05 | 2006-11-22 | Confoti Inc | Konfetti mit fotografischen bildern auf seiner oberfläche |
-
2004
- 2004-02-11 FR FR0401329A patent/FR2865957B1/fr not_active Expired - Fee Related
-
2005
- 2005-02-11 ES ES05717624T patent/ES2332004T3/es not_active Expired - Lifetime
- 2005-02-11 PL PL05717624T patent/PL1718441T3/pl unknown
- 2005-02-11 CA CA 2555588 patent/CA2555588A1/fr not_active Abandoned
- 2005-02-11 BR BRPI0507566-1A patent/BRPI0507566A/pt not_active IP Right Cessation
- 2005-02-11 AT AT05717624T patent/ATE439960T1/de not_active IP Right Cessation
- 2005-02-11 SI SI200530827T patent/SI1718441T1/sl unknown
- 2005-02-11 WO PCT/FR2005/000335 patent/WO2005077622A2/fr not_active Ceased
- 2005-02-11 DE DE200560016081 patent/DE602005016081D1/de not_active Expired - Lifetime
- 2005-02-11 EP EP05717624A patent/EP1718441B1/de not_active Expired - Lifetime
- 2005-02-11 US US10/589,001 patent/US20080042425A1/en not_active Abandoned
Also Published As
| Publication number | Publication date |
|---|---|
| SI1718441T1 (sl) | 2010-01-29 |
| WO2005077622A3 (fr) | 2005-12-08 |
| EP1718441A2 (de) | 2006-11-08 |
| FR2865957B1 (fr) | 2006-04-28 |
| DE602005016081D1 (de) | 2009-10-01 |
| US20080042425A1 (en) | 2008-02-21 |
| WO2005077622A2 (fr) | 2005-08-25 |
| FR2865957A1 (fr) | 2005-08-12 |
| CA2555588A1 (fr) | 2005-08-25 |
| ES2332004T3 (es) | 2010-01-22 |
| ATE439960T1 (de) | 2009-09-15 |
| PL1718441T3 (pl) | 2010-02-26 |
| BRPI0507566A (pt) | 2007-07-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| RU2408466C2 (ru) | Ценная бумага и способ ее изготовления | |
| CN1652945B (zh) | 防伪元件及其制造方法 | |
| CA2470996A1 (en) | Security element and methods for producing it | |
| CA2761781A1 (fr) | Procede de fabrication d'un element de securite pour document de securite | |
| FR2865957A1 (fr) | Procede de fabrication et de decoupe d'elements de format relativement petit, dispositifs correspondants, elements et feuilles comportant lesdits elements | |
| JP5182142B2 (ja) | シート状印刷物及びその製造方法 | |
| JPS6317095A (ja) | 改変防止用素材 | |
| EP2049731B1 (de) | Sicherheitselement von relativ geringem format mit einem durchgangsloch und blech damit | |
| EP1716289B1 (de) | Verhältnismässig kleine sicherheitselemente, deren herstellungsverfahren sowie sie umfassende folie und wertschrift | |
| EP1871952B1 (de) | Hochsicheres papier und herstellungsverfahren | |
| WO2008032411A1 (fr) | Dispositif pour la discrimination d'une authenticité et substrat permettant la discrimination d'une authenticité | |
| JP2021506622A (ja) | 抄紙機が製作した孔部上へのセキュリティデバイスの表面適用方法 | |
| KR101164549B1 (ko) | 게임데이터 위변조 방지를 위한 즉석식 복권의 인쇄구조 및 그 인쇄방법 | |
| CN102691226B (zh) | 一种带有视窗和水印的防伪纸的制备方法 | |
| EP0599675B1 (de) | Sicherheitsbahn, insbesondere zur Anwendung als Passdeckblatt | |
| FR2960005A1 (fr) | Document de securite comportant un filigrane ou pseudo-filigrane, une image combinee et une trame de revelation, et procedes associes. | |
| JP5182141B2 (ja) | シート状印刷物及びその製造方法 | |
| JP5636737B2 (ja) | 偽造防止用紙 | |
| JP3166885U (ja) | 葉書用模様紙および葉書 | |
| JP2016043551A (ja) | 耐剥離性印刷物 | |
| Luff | What Philately Teaches | |
| JP2016002693A (ja) | 偽造防止媒体 | |
| TWM434288U (en) | Roll-type memo paper | |
| JP2004306532A (ja) | 名刺、名刺用原紙および、名刺の作成方法 | |
| CZ26463U1 (cs) | Výherní los |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20060911 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| 17Q | First examination report despatched |
Effective date: 20070518 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 602005016081 Country of ref document: DE Date of ref document: 20091001 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: KIRKER & CIE S.A. |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2332004 Country of ref document: ES Kind code of ref document: T3 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20090819 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091219 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091221 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091119 |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E006946 Country of ref document: HU |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20100520 |
|
| BERE | Be: lapsed |
Owner name: ARJOWIGGINS SECURITY Effective date: 20100228 Owner name: ETIVOL Effective date: 20100228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100301 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091120 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100228 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20120221 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100211 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090819 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: HU Payment date: 20130301 Year of fee payment: 9 Ref country code: SE Payment date: 20130219 Year of fee payment: 9 Ref country code: FR Payment date: 20130301 Year of fee payment: 9 Ref country code: ES Payment date: 20130227 Year of fee payment: 9 Ref country code: DE Payment date: 20130219 Year of fee payment: 9 Ref country code: GB Payment date: 20130218 Year of fee payment: 9 Ref country code: CH Payment date: 20130220 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20130219 Year of fee payment: 9 Ref country code: PL Payment date: 20130124 Year of fee payment: 9 Ref country code: SI Payment date: 20130131 Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602005016081 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20140901 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20140211 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140228 Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140901 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140228 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20141031 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602005016081 Country of ref document: DE Effective date: 20140902 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140212 Ref country code: HU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140212 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140212 |
|
| REG | Reference to a national code |
Ref country code: SI Ref legal event code: KO00 Effective date: 20141008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140902 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140211 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140228 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20150327 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140212 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140211 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: LAPE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140211 |