EP1568639B1 - Procédé et dispositif pour la formation de piles de produits disposées côte à côte - Google Patents
Procédé et dispositif pour la formation de piles de produits disposées côte à côte Download PDFInfo
- Publication number
- EP1568639B1 EP1568639B1 EP04090073A EP04090073A EP1568639B1 EP 1568639 B1 EP1568639 B1 EP 1568639B1 EP 04090073 A EP04090073 A EP 04090073A EP 04090073 A EP04090073 A EP 04090073A EP 1568639 B1 EP1568639 B1 EP 1568639B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- separating
- product
- individual
- paper sheets
- stack
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 19
- 238000003825 pressing Methods 0.000 claims description 13
- 230000015572 biosynthetic process Effects 0.000 abstract description 2
- 238000009825 accumulation Methods 0.000 abstract 4
- 239000000123 paper Substances 0.000 description 19
- 238000003860 storage Methods 0.000 description 12
- 238000004519 manufacturing process Methods 0.000 description 5
- 239000000463 material Substances 0.000 description 3
- 238000000926 separation method Methods 0.000 description 3
- 238000013022 venting Methods 0.000 description 3
- 230000001133 acceleration Effects 0.000 description 2
- 238000003892 spreading Methods 0.000 description 2
- 230000000740 bleeding effect Effects 0.000 description 1
- 239000003795 chemical substances by application Substances 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000002950 deficient Effects 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000001125 extrusion Methods 0.000 description 1
- 239000011888 foil Substances 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 238000009423 ventilation Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H31/00—Pile receivers
- B65H31/32—Auxiliary devices for receiving articles during removal of a completed pile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H31/00—Pile receivers
- B65H31/30—Arrangements for removing completed piles
- B65H31/3036—Arrangements for removing completed piles by gripping the pile
- B65H31/3045—Arrangements for removing completed piles by gripping the pile on the outermost articles of the pile for clamping the pile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/42—Piling, depiling, handling piles
- B65H2301/421—Forming a pile
- B65H2301/4217—Forming multiple piles
- B65H2301/42172—Forming multiple piles simultaneously
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/42—Piling, depiling, handling piles
- B65H2301/422—Handling piles, sets or stacks of articles
- B65H2301/4223—Pressing piles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/42—Piling, depiling, handling piles
- B65H2301/422—Handling piles, sets or stacks of articles
- B65H2301/4224—Gripping piles, sets or stacks of articles
- B65H2301/42242—Gripping piles, sets or stacks of articles by acting on the outermost articles of the pile for clamping the pile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2601/00—Problem to be solved or advantage achieved
- B65H2601/20—Avoiding or preventing undesirable effects
- B65H2601/21—Dynamic air effects
- B65H2601/211—Entrapping air in or under the material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2701/00—Handled material; Storage means
- B65H2701/10—Handled articles or webs
- B65H2701/17—Nature of material
- B65H2701/176—Cardboard
Definitions
- the invention relates to a device for forming a plurality of product stacks arranged next to one another from an incoming product stream of paper sheets or the like, comprising a storage area for receiving the incoming paper sheets or the like and forming product stacks, at least one separating element for each product stack to form a gap between a respective product stack that can be removed and subsequently incoming paper sheets or the like, as well as means for squeezing air inclusions from the product stacks that can be removed.
- the invention relates to a method for forming a plurality of juxtaposed product stacks from an incoming product stream of paper sheets or the like, comprising the steps of: collecting and stacking the incoming paper sheets or the like in a storage area, wherein a plurality of product stacks are formed side by side at the same time, separating the product stacks that can be removed by incoming paper sheets or the like by forming a gap between a respective transportable product stack and subsequently incoming paper sheets or the like by means of separating elements, squeezing air inclusions from the product stowable product by suitable means.
- Such devices and methods are used in particular in the production of stacks of paper, cardboard or other stackable materials, such as films.
- stacks are produced in usually mehmutzigen production machines.
- longitudinal and / or transverse cutting of material webs continuously forms so-called giants in the form of sheet layers or sheet stacks.
- a mehmutzigen production machine several of these giant are close together and form a Riesstrang.
- This Riesstrang is stored in a collection station, for example, the storage area.
- suitable means expediently a tong system, the giant strand is pulled onto a device for conveying the giant transversely to its Antransportides or deposited on this.
- the stack venting takes place during the conveying process on intermediate conveyors.
- the device has, in addition to a clamping device, an air-spreading device for each conveying direction, which cooperates such that the stack held by the clamping device on the intermediate conveyor is moved under the corresponding air-spreading device pressing on the stack.
- JP 07137921 deals with a device in which a vent roller, which is arranged on a support arm, can be lowered onto the stack to be vented. By moving the support arm relative to stack the latter is vented.
- a device of the type mentioned above in that the means for squeezing air inclusions from the product stacks wegtransporttransportrise consists of several individual elements, each separating element is associated with a single element.
- a particularly compact device is created, which is also easy to retrofit to existing devices.
- the device according to the invention is particularly inexpensive to produce, since the dividers exist anyway with all the required degrees of freedom, namely rotation, pivot and movement axes in the device, so that a retrofit is particularly easy and inexpensive to implement.
- each separating finger is formed as part of the separating element pivotable about an axis of rotation, wherein the separating finger is spring-loaded.
- each individual element for pressing air inclusions perpendicular to the transport plane projects beyond the separating finger in the direction of the transport plane. This avoids that the separating finger rests in a lowered position on the uppermost sheet of a transportable stack and causes marks by rubbing. The quality of the removable stack is therefore improved.
- the object is achieved by a method with the steps mentioned above in that the extrusion of the air pockets for each product stack by a consisting of several individual elements means in which each separating element is assigned a single element, is carried out separately. This individual bleeding of each individual stack of a giant strand slippage of individual sheets of a stack is particularly effective prevented.
- the devices shown in the figures or the method described with reference to the figures are used for venting formed from individual sheets of paper or the like stacks.
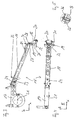
- FIG. 1 shows a device 10 for forming a plurality of juxtaposed product stacks 11 from an incoming product stream 12 of paper sheets 13 or the like.
- The preferably transported in a scale formation in a transport plane E paper sheets 13 run from a (not shown) multi-purpose production machine in Antransporteurs (arrow A) in a storage area 14, where the incoming paper sheets 13 are stacked into a product stack 11.
- the device 10 further comprises at least one separating element 15, wherein the number of separating elements 15 corresponds at least to the number of product stacks 11 of a giant strand formed from a plurality of juxtaposed product stacks.
- at least one separating element 15 is assigned to each product stack 11.
- each product stack 11 can also be assigned two or more separating elements 15.
- Each separating element 15 is arranged above the transport plane E and has a support element 17, a separating lever 18 and a separating finger 19. At each separating element 15, preferably in the region of each separating finger 19, at least one individual element 20 is arranged directly and directly as a means 16 for squeezing air inclusions.
- the support member 17 is pivotally movable about an axis of rotation 21 and in and against the Antransportides the product stream 12 according to arrow A.
- the support member 17 is rotatably mounted on a shaft 22, e.g. by means of a clamping or quick release, arranged, which in turn is driven in rotation by means of conventional drive means.
- the support element 17 itself can also be driven pivotably.
- a free end 23 of the support member 17 of the separating lever 18 is pivotally mounted about the axis of rotation 24.
- the release lever 18 is spring-loaded.
- a spring element 25 is provided for this purpose, which is arranged on the one hand on the support member 17 or on a stationary part of the device 10 and on the other hand on the separating lever 18.
- the stop 26 is arranged in the Antransportides behind the rotation axis 24 and movable from a stop position to a release position and vice versa.
- the locking means may e.g. a screw which is rotatable in a thread of the bore 36, such that the separating element 18 is fixed, ie without relative movement to the support member 17, arranged thereon.
- the separating finger 19 is designed such that it can pivot about an axis of rotation 28 relative to the separating lever 18.
- the separating finger 19 is optionally also spring-loaded, wherein a spring element 29 on the one hand on the separating lever 18 and on the other hand on the separating finger 19th is fastened such that the separating finger 19 by means of the spring force counterclockwise about the rotation axis 28 is pivotable.
- the pivoting movement is limited by a stop 30, wherein the stopper 30 can be brought from a stop position into a release position and vice versa.
- the separating finger 19 is formed substantially L-shaped. On a long leg 31, the single element 20 is arranged. The short leg 32 is pointed toward the free end, so quasi ramped, shaped to facilitate the run-in or emergence of the incoming product stream 12.
- Each of the individual elements 20 for squeezing air inclusions comprises at least one pressure roller and / or a brush element.
- the single element 20 can also consist of two or more identical or different elements for pressing or pressing.
- a plurality of individual elements 20 may be associated with a separating element 15 or each separating finger 19.
- Other stationary or rotating pressing or pressing elements can also be used.
- the individual elements 20 may be e.g. Also be designed as a plate-shaped pressure elements, each having a cavity. Such pressing elements can be acted upon in the cavity with compressed air. Through openings on the side facing the stack of the pressure element, the compressed air can escape, so that virtually contactless pressure on the stack can be applied to squeeze the air bubbles within the stack.
- Each individual element 20 is firmly connected to the separating element 15 or more precisely to the separating finger 19. This means that each movement in the linear and rotating directions of the separating finger 19 is carried out in the same way by the single element 20.
- the single element 20 is preferably releasably secured in the region of the long leg 31 at this.
- the position or position of the individual element 20 to the long leg 31 is selected such that the individual element 20 extends perpendicular to the transport plane E (see Figures 3 and 4, plane E is spanned by the coordinates X and Z) in the direction of the same over the leg 31 , so that when lowering the separating element 15 on the product stack 11 to be transported away, the single element 20 is first placed on the product stack 11. In transport direction (Arrow A) of the product flow 12, the single element 20 is arranged behind the leg 31.
- the individual element 20 does not have to be arranged on the separating element 15 or on the separating finger 19. Rather, the single element 20 may be stored independently.
- the individual element 20 may be pivotable about the rotation axis 21 on a separate lever (not shown) on the shaft 22.
- each separating element 15 adjacent to a lever associated with the individual element 20 disposed thereon.
- Each separating element 15 can also be assigned a plurality of individual elements 20, for example on both sides.
- the separation of separator 15 on the one hand and single element lever 20 on the other hand has the advantage that e.g. in the case of a defect, the replacement of the defective parts or the maintenance thereof is simplified.
- the contact pressure of the individual elements 20 can then be adjusted independently of the separating element 15.
- the paper sheets 13 cut from a material web are collected in the storage area 14, eg in a collection box.
- the separating element 15 lowers, so that the short leg 32 of the separating finger 19 rests on the top sheet of the product stack 11 (see Figure 6a).
- a gripping means such as a forceps system 33 in front of the storage area 14.
- the individual elements 20 of each separating element 15 are in Antransportides according to arrow A behind the product stack 11 to be transported over.
- the pliers system 33 grips the product stack 11 (also called a package).
- the separating element 15 is raised for this purpose by pivoting, so that there is no contact between the separating element 15 and the product stack 11. Subsequently, the pliers system 33 pulls the product stack 11 from the storage area 14. The simultaneously and continuously incoming paper sheets 13 rest on the short leg 32 of the separating finger 19. While the product stack 11 is pulled out of the storage area 14, a rake 34 is simultaneously tracked at the same speed to the incoming and initially only on the separation finger 19 supported paper sheets to support 13 (see Figure 6c). When the product stack 11 is at least partially pulled out of the storage area 14, the separating element 15 lowers again, so that the individual element 20 projecting beyond the separating finger 19 touches the uppermost sheet of the product stack 11 (see FIG. 6d).
- the product stack 11 is further pulled away below the single element 20, whereby the air pockets located in the product stack 11 are squeezed out.
- the single element 20 prevents at the same time that the separating finger 19 itself rests on the product stack 11, so that chafing or the like is prevented by a gap 35 between separation finger 19 and product stack 11 is formed (see in particular Figure 2).
- the rake 34 reaches its end position in front of the separating finger 19.
- the separating element 15 drops with its separating finger 19 to the level of the rake 34.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Sheets, Magazines, And Separation Thereof (AREA)
- Making Paper Articles (AREA)
- Container Filling Or Packaging Operations (AREA)
- Pile Receivers (AREA)
Claims (13)
- Dispositif pour former plusieurs piles de produits (11) disposées côte à côte, à partir d'un flux de produits (12) arrivant, constitué de feuilles de papier (13) ou produits analogues, dispositif comprenant une zone de dépôt (14) pour la réception des feuilles de papier (13) ou produits analogues, qui arrivent, et la formation de piles de produits (11) aptes à être évacuées, au moins un élément de séparation (15) pour chaque pile de produits (11), destiné à former un interstice entre une pile de produits (11) respective, apte à être évacuée, et des feuilles de papier (13) ou produits analogues, qui arrivent en succession, ainsi que des moyens (16) pour expulser des inclusions d'air des piles de produits (11) aptes à être évacuées, caractérisé en ce que le moyen (16) pour expulser des inclusions d'air des piles de produits (11) aptes à être évacuées, se compose de plusieurs éléments individuels (20), un élément individuel (20) étant alors associé à chaque élément de séparation (15).
- Dispositif selon la revendication 1, caractérisé en ce que sur chaque élément de séparation (15), est disposé un élément individuel (20) indépendant vis-à-vis des autres éléments individuels (20).
- Dispositif selon la revendication 1 ou 2, caractérisé en ce que chaque élément de séparation (15) est disposé au-dessus du plan de transport (E) du flux de produits (12) et est constitué essentiellement d'un élément d'appui (17), d'un levier de séparation (18) ainsi que d'un doigt de séparation (19).
- Dispositif selon la revendication 3, caractérisé en ce que l'élément d'appui (17) est conçu pivotant autour d'un axe de rotation (21) et déplaçable dans le sens du transport d'amenée (A) du flux de produits (12) et en sens inverse.
- Dispositif selon la revendication 3 ou 4, caractérisé en ce que le levier de séparation (18) est conçu pivotant autour d'un axe de rotation (24), le levier de séparation (18) étant alors sollicitable par un ressort.
- Dispositif selon l'une des revendications 3 à 5, caractérisé en ce que le doigt de séparation (19) est conçu pivotant autour d'un axe de rotation (28), le doigt de séparation (19) étant alors sollicitable par un ressort.
- Dispositif selon l'une des revendications 1 à 6, caractérisé en ce que chaque élément individuel (20) destiné à expulser des inclusions d'air comprend au moins un rouleau presseur et/ou un élément en forme de brosse.
- Dispositif selon l'une des revendications 3 à 7, caractérisé en ce que chaque élément individuel (20) est relié rigidement au doigt de séparation (19), de telle manière que tout déplacement du doigt de séparation (19) soit obligatoirement exécuté en synchronisme par l'élément individuel (20).
- Dispositif selon l'une des revendications 1 à 8, caractérisé en ce que chaque élément individuel (20) destiné à expulser des inclusions d'air fait saillie au-delà du doigt de séparation (19), en direction du plan de transport (E), perpendiculairement au plan de transport (E).
- Procédé pour former plusieurs piles de produits (11) disposées côte à côte, à partir d'un flux de produits (12) arrivant, constitué de feuilles de papier (13) ou produits analogues, comprenant les étapes de :- rassemblement et empilement des feuilles de papier (13) ou produits analogues, qui arrivent, dans une zone de dépôt (14), plusieurs piles de produits (11) étant alors formées en même temps l'une à côté de l'autre,- séparation, au moyen d'éléments de séparation (15), des piles de produits (11), aptes à être évacuées, de feuilles de papier (13) ou produits analogues, qui arrivent, par formation d'un interstice entre une pile de produits (11) respective, apte à être évacuée, et des feuilles de papier (13) ou produits analogues, qui arrivent en succession,- expulsion d'inclusions d'air des piles de produits (11) aptes à être évacuées, à l'aide de moyens adaptés (16),caractérisé en ce que l'expulsion des inclusions d'air est effectuée séparément pour chaque pile de produits (11) par un moyen constitué de plusieurs éléments individuels, un élément individuel étant associé à chaque élément de séparation.
- Procédé selon la revendication 10, caractérisé en ce que sur chaque pile de produits (11) est exercée une pression propre pour l'expulsion des inclusions d'air.
- Procédé selon la revendication 10 ou 11, caractérisé en ce que des différences de hauteur des piles de produits (11) d'une chaîne de rames constituée de plusieurs piles de produits (11), qui se trouve dans la zone de dépôt (14), sont compensées.
- Procédé selon l'une des revendications 10 à 12, caractérisé en ce que les éléments de séparation (15) sont relevés pendant l'expulsion des inclusions d'air, afin qu'il se forme un interstice entre la feuille la plus haute d'une pile de produits (11), apte à être évacuée, et l'élément de séparation (15).
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP04090073A EP1568639B1 (fr) | 2004-02-27 | 2004-02-27 | Procédé et dispositif pour la formation de piles de produits disposées côte à côte |
| AT04090073T ATE344209T1 (de) | 2004-02-27 | 2004-02-27 | Vorrichtung und verfahren zur bildung mehrerer nebeneinander angeordneter produktstapel |
| DE502004001895T DE502004001895D1 (de) | 2004-02-27 | 2004-02-27 | Vorrichtung und Verfahren zur Bildung mehrerer nebeneinander angeordneter Produktstapel |
| PT04090073T PT1568639E (pt) | 2004-02-27 | 2004-02-27 | Dispositivo para a criação de várias pilhas dispostas em paralelo |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP04090073A EP1568639B1 (fr) | 2004-02-27 | 2004-02-27 | Procédé et dispositif pour la formation de piles de produits disposées côte à côte |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1568639A1 EP1568639A1 (fr) | 2005-08-31 |
| EP1568639B1 true EP1568639B1 (fr) | 2006-11-02 |
Family
ID=34746053
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP04090073A Expired - Lifetime EP1568639B1 (fr) | 2004-02-27 | 2004-02-27 | Procédé et dispositif pour la formation de piles de produits disposées côte à côte |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP1568639B1 (fr) |
| AT (1) | ATE344209T1 (fr) |
| DE (1) | DE502004001895D1 (fr) |
| PT (1) | PT1568639E (fr) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102006029342A1 (de) * | 2006-06-23 | 2008-01-03 | Bielomatik Leuze Gmbh + Co.Kg | Sammel- und Fördervorrichtung für durch Blattlagen gebildete Stapel |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3046107C2 (de) * | 1980-12-06 | 1982-11-18 | Bielomatik Leuze Gmbh + Co, 7442 Neuffen | Vorrichtung zum Ablegen von Bogen zu einem Stapel |
| DE3403209A1 (de) * | 1983-02-12 | 1984-08-16 | E.C.H. Will (Gmbh & Co), 2000 Hamburg | Einrichtung zur beseitigung von lufteinschluessen aus papierstapeln |
| DE3540203C2 (de) * | 1985-11-13 | 1993-12-09 | Will E C H Gmbh & Co | Vorrichtung zum Fördern von Papierstapeln |
| JP2547175B2 (ja) * | 1993-11-12 | 1996-10-23 | 株式会社永井機械製作所 | 紙揃装置 |
| DE19523699A1 (de) * | 1995-06-29 | 1997-01-09 | Will E C H Gmbh & Co | Vorrichtung zum Entfernen von Lufteinschlüssen aus Papierstapeln |
| DE10208309A1 (de) * | 2002-02-27 | 2003-09-04 | Will E C H Gmbh & Co | Vorrichtung zum Bilden und Abfördern von Bogenstapeln mit einem Trennband |
-
2004
- 2004-02-27 PT PT04090073T patent/PT1568639E/pt unknown
- 2004-02-27 EP EP04090073A patent/EP1568639B1/fr not_active Expired - Lifetime
- 2004-02-27 AT AT04090073T patent/ATE344209T1/de not_active IP Right Cessation
- 2004-02-27 DE DE502004001895T patent/DE502004001895D1/de not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| PT1568639E (pt) | 2007-02-28 |
| ATE344209T1 (de) | 2006-11-15 |
| DE502004001895D1 (de) | 2006-12-14 |
| EP1568639A1 (fr) | 2005-08-31 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2072430B1 (fr) | Dispositif de saisie de paquet pour un dispositif de palettisation et procédé de palettisation de paquets | |
| DE69702274T2 (de) | Vorrichtung zum Sammeln und Stapeln von Schichtwerkstoffen, und ein Stapelverfahren | |
| EP3603948B1 (fr) | Installation de fabrication de carton ondulé | |
| EP2457858A1 (fr) | Dispositif et méthode pour la formation de paquets de produits imprimés | |
| DE3126807A1 (de) | Stangenstapler fuer gefalzte druckbogen | |
| EP2028732B1 (fr) | Dispositif de production et de confection consécutive d'une section de câble sur son extrémité avant et arrière | |
| DE2508745C2 (de) | Vorrichtung zum Aufstauen vereinzelt mittels einer Transportvorrichtung zugeförderter Papierbögen zu Stapeln und zum Weitertransportieren dieser Stapel | |
| DE3540203C2 (de) | Vorrichtung zum Fördern von Papierstapeln | |
| DE102020115827A1 (de) | Verfahren zum Ver- und/oder Bearbeiten eines Stapels blattförmigen Guts sowie Schneidanlage | |
| EP0309745B1 (fr) | Dispositif pour empiler des articles imprimés arrivant de façon continue en formation imbriquée | |
| EP0931748B1 (fr) | Plieuse sans pointure pour machines rotatives à imprimer | |
| AT516092B1 (de) | Vorrichtung und Verfahren zum Transport von schlauchförmigen Sackkörpern | |
| EP0368028B1 (fr) | Méthode et dispositif de fabrication de couches en partant de bandes plus larges ayant une couche de protection | |
| EP1568639A1 (fr) | Procédé et dispositif pour la formation de piles de produits disposées côte à côte | |
| EP4363362A1 (fr) | Appareil et procédé pour diviser une pile de feuilles en rames comprenant un nombre spécifié de feuilles | |
| DE102013001778A1 (de) | Überwachungsverfahren zur Kollisionsvermeidung einer Stanzmaschine mit Bremsbürste | |
| DE602004011618T2 (de) | Verfahren und Vorrichtung zur Aufnahme eines Blattes in einer Maschine zur Bearbeitung von brettförmigem Gut | |
| EP2998258B1 (fr) | Dispositif d'enroulement de feuille pour une machine d'emballage | |
| DE102009045319B4 (de) | Formateinstellvorrichtung | |
| EP2323938B1 (fr) | Dispositif de collecte et de transport d'empilements formés de couches de feuilles | |
| DE118311C (fr) | ||
| EP1712471B1 (fr) | Dispositif et procédé d'emballage d'articles | |
| DE19607508C1 (de) | Auspackmaschine für Rollen, insbes. Druckpapierrollen | |
| EP2436623B1 (fr) | Procédé et dispositif pour enlever une rangée de piles | |
| EP2341779B1 (fr) | Procédé et dispositif de séparation de morceaux de produits coupés |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK |
|
| 17P | Request for examination filed |
Effective date: 20060222 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| GRAC | Information related to communication of intention to grant a patent modified |
Free format text: ORIGINAL CODE: EPIDOSCIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20061102 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061102 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061102 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061102 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061102 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 502004001895 Country of ref document: DE Date of ref document: 20061214 Kind code of ref document: P |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20061220 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070202 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070202 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070213 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070228 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20070122 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20070803 |
|
| BERE | Be: lapsed |
Owner name: E.C.H. WILL G.M.B.H. Effective date: 20070228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070203 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20080310 Year of fee payment: 5 Ref country code: FI Payment date: 20080227 Year of fee payment: 5 Ref country code: GB Payment date: 20080219 Year of fee payment: 5 Ref country code: IT Payment date: 20080221 Year of fee payment: 5 Ref country code: NL Payment date: 20080226 Year of fee payment: 5 Ref country code: PT Payment date: 20080124 Year of fee payment: 5 Ref country code: SE Payment date: 20080219 Year of fee payment: 5 Ref country code: SK Payment date: 20080206 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20080226 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20080215 Year of fee payment: 5 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080229 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080229 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061102 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070227 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MM4A Free format text: LAPSE DUE TO NON-PAYMENT OF FEES Effective date: 20090827 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070503 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061102 |
|
| EUG | Se: european patent has lapsed | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20090227 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090227 Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090827 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090227 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20090901 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20091030 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090227 Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090901 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090901 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090227 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090302 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090228 |