EP1362791B1 - Vorrichtung und Verfahren zum Kennzeichnen von Zigarettenpackungen - Google Patents
Vorrichtung und Verfahren zum Kennzeichnen von Zigarettenpackungen Download PDFInfo
- Publication number
- EP1362791B1 EP1362791B1 EP03004932A EP03004932A EP1362791B1 EP 1362791 B1 EP1362791 B1 EP 1362791B1 EP 03004932 A EP03004932 A EP 03004932A EP 03004932 A EP03004932 A EP 03004932A EP 1362791 B1 EP1362791 B1 EP 1362791B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- station
- marking
- batch
- cigarette
- stack
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 235000019504 cigarettes Nutrition 0.000 title claims abstract description 113
- 238000000034 method Methods 0.000 title claims abstract description 21
- 238000007639 printing Methods 0.000 claims abstract description 19
- 238000000608 laser ablation Methods 0.000 claims abstract description 5
- 238000002372 labelling Methods 0.000 claims description 24
- 238000004806 packaging method and process Methods 0.000 claims description 9
- 229920000298 Cellophane Polymers 0.000 claims description 7
- IHQKEDIOMGYHEB-UHFFFAOYSA-M sodium dimethylarsinate Chemical class [Na+].C[As](C)([O-])=O IHQKEDIOMGYHEB-UHFFFAOYSA-M 0.000 claims description 3
- 239000002985 plastic film Substances 0.000 abstract 1
- 229920006255 plastic film Polymers 0.000 abstract 1
- 230000004888 barrier function Effects 0.000 description 5
- 238000004519 manufacturing process Methods 0.000 description 2
- 238000000926 separation method Methods 0.000 description 2
- 230000006641 stabilisation Effects 0.000 description 2
- 238000011105 stabilization Methods 0.000 description 2
- 238000011144 upstream manufacturing Methods 0.000 description 2
- 206010044565 Tremor Diseases 0.000 description 1
- 238000002679 ablation Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 239000011888 foil Substances 0.000 description 1
- 125000000524 functional group Chemical group 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 238000007641 inkjet printing Methods 0.000 description 1
- 238000010330 laser marking Methods 0.000 description 1
- 230000005415 magnetization Effects 0.000 description 1
- 238000007645 offset printing Methods 0.000 description 1
- 210000000056 organ Anatomy 0.000 description 1
- 238000012856 packing Methods 0.000 description 1
- 230000003068 static effect Effects 0.000 description 1
- 238000000859 sublimation Methods 0.000 description 1
- 230000008022 sublimation Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
- B65B61/26—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for marking or coding completed packages
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B19/00—Packaging rod-shaped or tubular articles susceptible to damage by abrasion or pressure, e.g. cigarettes, cigars, macaroni, spaghetti, drinking straws or welding electrodes
- B65B19/02—Packaging cigarettes
- B65B19/22—Wrapping the cigarettes; Packaging the cigarettes in containers formed by folding wrapping material around formers
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10S—TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10S101/00—Printing
- Y10S101/30—Special article printing with article controlled operation
Definitions
- the present invention relates to an apparatus and a method for Labeling of cigarette packs.
- the present invention relates The invention relates to a device and a method for identifying Cigarette packs containing information for manufacturers and / or distributors and / or Customers, for example with information about production time, aggregate, company, Authenticity, delivery history or customer information in plain text or encrypted.
- Cigarette pack imprinted or otherwise applied to this, so that the pack had to be opened to read the information.
- Methods have been known to provide information on the outside of the Apply cigarette pack, for example by inkjet printing or Laser marking. There is basically the requirement that the flow of Cigarette packs during production as possible not interrupted or is stopped.
- WO 01/54986 discloses a method and an arrangement for characterizing Cigarette packs, the cigarette packs on a belt conveyor rest on a tagging device, such as a laser or a printing unit to be guided over. While the label is a stable hold of the cigarette packs on the belt conveyor not guaranteed. This can lead to inaccuracies in the labeling.
- WO 02/04297 A1 discloses a device for marking, in the opposite lying side surfaces of the cigarette packs of two parallel Clamped endless belts and passed to a printing unit over.
- printed can be either only from the endless belts projecting side sections a cigarette pack or not clamped by the conveyor belts Side faces.
- comparatively large side surfaces of a Cigarette pack will not be labeled what the Limits labeling options.
- DE 100 04 022 A1 discloses a method and a device for attaching Codes on cigarette packs, the or the either comparable to WO 02/04297 A1 is formed or when the cigarette packs in a bag Dry turrets are guided in circles and labeled with a laser. Also at this arrangement is subject to the area available for marking device-related restrictions.
- the object of the present invention is the device and the method according to WO 02/04297 A1 to further form that the labeling of cigarette packs made even more reliable and still fewer restrictions, in particular as regards labeling for Available area, may be subject.
- a device for identifying cigarette packets comprises a transport device for the promotion of Cigarette packages to a labeling station for the identification of Cigarette packs. While in the prior art, the cigarette packs predominantly individually guided past an identification device, According to the invention, the cigarette packs in batches to one Labeling station transferred and marked there. According to the present Invention detects the transport device thus a stack of each other attached, aligned cigarette packs and brings them to Identification station, where the transport device releases the stack again and the released cigarette packs on at least one exposed area be labeled.
- the adjoining, aligned Cigarette packs existing stack has a certain inherent stability, so that mechanical disturbances, for example of conveyors caused tremors, jerky movements, etc., a lesser Have an influence on the positioning of cigarette packs.
- mechanical disturbances for example of conveyors caused tremors, jerky movements, etc.
- a lesser Have an influence on the positioning of cigarette packs According to the invention thus less holding and stabilization effort required to the To position cigarette packets for identification reliably.
- the cigarette packs only on comparatively small areas or not at all to pinch while these be marked, so that usually at least three surfaces of a Cigarette pack are available for labeling.
- the handling of the packs in addition as a stack because thereby the Dead times during transport can be reduced.
- labeling fields of e.g. better exploit a laser because this Labeling fields can extend over several package side surfaces.
- the number of packs in the stack should therefore be the size of the label field be adjusted.
- the cigarette packs are in the labeling with a Side surface on a substantially flat support surface, for example, on a belt conveyor, a plate or a table-like clamping device. Consequently lie in the shared stack side faces of neighboring Cigarette packs automatically to each other over the entire surface, so that comparatively large static friction act, the shifting or Slipping of the cigarette packs, caused for example by prevent mechanical interference. It is advantageous that the cigarette packs can be positioned even more reliable in a simple way.
- the cigarette packs are with their during the labeling Narrow sides on the substantially flat support surface, so are upright arranged. While a single upright arranged cigarette pack is relatively susceptible to tipping, is the Kippiffkeit a stack of upright arranged and adjacent, aligned Cigarette packs significantly lower. Thus, according to the invention in particular narrow sides, in particular those of the support opposite Narrow sides of cigarette packs at comparatively low holding and Stabilization effort can be reliably marked.
- Preferably comprises at least as many cigarette packs, that the length of the stack in the transport direction is greater than or equal to the horizontal format a cigarette pack is.
- a stack in the marking station is preferred in the marking additionally fixed so that the cigarette packs at least during the Marking can not slip or tilt substantially. Consequently an even more reliable positioning is achieved.
- the Transport device itself or an additional fixing device used become.
- the stack in the labeling station can not to clamping sections of a cigarette packet, touched, be mechanically guided on one side abut a stop or in other Be fixed by mechanical force.
- the power to fix Can be used on all cigarette packs in a stack in the Marking station attack, but the power to fix can only on attack a few selected cigarette packs of a stack, in particular at the front and rear, viewed in the conveying direction, cigarette packs of the released stack.
- the fixing device for transporting or fixing device is preferred adjustable designed to move between a rest position in which not all about concealed by transport organs side surfaces of the cigarette packs of the Stack can be accessed substantially unhindered, and one Fixing position, in which the transport device or the fixing device at least sections act on side surfaces of cigarette packs, back and to be moved.
- the transport device is designed to not only a stack of to capture and align adjacent aligned cigarette packs but at least one more comparable stack, particularly preferred to capture only one more comparable stack and to transport. This advantageously increases the throughput of the invention Contraption.
- the transport device can at least two stacks, in particular during the marking, with in Apply substantially the same forces.
- the Transport device as at least two stack clamping clamping device, educated.
- the marking device and / or the stack while marking stationary which is even more accurate Positioning allows for labeling.
- the stack and the marking device become relative moved to each other, preferably the stack or Identification device is stationary and thus accurately positioned.
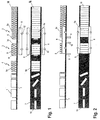
- Fig. 1 shows an apparatus for Marking of cigarette packs according to the present invention in one Starting position in a side view and in a plan view. Shown is a Detail of a more comprehensive cigarette packaging machine, in which the Cigarette packs 1 continuously in a stream of cigarette packs of right to left by means of a conveyor (not shown) to the Support surface 7 are promoted. As shown in Fig. 1, are the Cigarette packs 1 on the support surface 7 edgewise with their narrow sides 19th on, so that the front sides are freely accessible laterally. The width of the support surface 7 is slightly larger in Fig. 1 than the length of a narrow side 19 to a to allow stable hold. The cigarette packs 1, however, can at least one side laterally beyond the edge of the support surface 7 protrude.
- the device according to FIG. 1 essentially comprises three stations, namely in the Processing order a Tarstaustation 2, a labeling station 3 and a separating station 4.
- the individually from each other or lying to each other incoming cigarette packs 1 accumulate at the fortification 2 and form there a stack of aligned with their broadsides, aligned Cigarette packs 9a.
- To block the incoming from the right stream of Cigarette packs is a projecting into the current barrier 6 is provided.
- the lock 6 by a known per se Clamping, holding or fixing to be replaced.
- the lock 6 is in the Drawing plane preferably stationary, but can, if the support surface 7 a Conveyor belt is, even slowed down with the conveyor belt 7 continue to run. It is essential a non-zero relative speed between lock 6 and Conveyor 7, to allow a damming.
- At least one identification device (not shown) arranged around the stack located in the identification station 3 9 to mark.
- identification Methods are used: printing, for example by means of inkjet printers, Laser printers, thermal sublimation printers, applied printing techniques, for example, offset printing, stamping, ablation techniques, for example laser ablation, or other surface manipulating methods, for example, local heat treatment, magnetization, labeling, etc.
- markings be applied of any kind, for example, as a barcode or as coded dot pattern.
- Cigarette packets 1 freely accessible, namely the two end faces 18 and upper narrow side 19. These side surfaces and about the side of the conveyor belt 7 protruding portions of the lower narrow side 19 are for marking in Essentially unhindered accessible.
- a separating station 4 provided in the five-piles, the straight from the identification station 3rd has been transferred.
- the separating station 4 do not work shown separating means on the cigarette packs of the downstream Stack 9p to separate the cigarette packs.
- the separating agents turn the cigarette packets 1 90 degrees in Longitudinal, so that the cigarette packs upright, on a narrow side 19 standing and preferably spaced from each other, leak from the device.
- Subordinate to the device are further handling units, for example a cellophaning station, not shown, and / or a packaging device, already cellophaniere cigarette packs, preferably as a five-pack be transported to unpack to bars.
- a cellophaning device can also be located upstream of that shown in FIG. 1 be arranged device shown and the marking on the Cellophane film or a marking surface attached thereto.
- the cigarette packs 1 of the stack 9 in the Identification station 3 of clamping devices 10, 11 fixed.
- the lock 6 and the clamping devices 10, 11 are movable to move in a first Position not to intervene in the flow of cigarette packets and around in one second position in the flow of cigarette packets to intervene To handle cigarette packs 1.
- the lock 6 and the clamping device 10, 11 can in particular be adjusted horizontally and / or vertically, pivoted or in be moved in another suitable manner.
- the transport device comprises two symmetrical to the support surface 7 arranged cuboid jaws 8, the the stacks release 9, 9a of cigarette packs in the first position and in the Capture second position, in particular laterally clamp, and transport.
- the two jaws 8 bridge the gap between the lock 6 and the clamping device 10 symmetrically and can in the Aufstaustation 2 and in the marking station 3 in the second position a take identical number of cigarette packs as a stack 9, 9a.
- the transport device basically any other number of cigarette packs 1 at a time grab and carry on.
- the Transport device 8 In addition to the jaws 8 and the adjusting means 12 includes the Transport device 8 a not shown motor adjustment means, so that the Transport device 8 from the initial position shown in FIG. 1 in the in Fig. 3 shown end position transferred and moved back. Below is described by way of example a mode of operation of a device according to the invention.
- the pent-up in the Aufstaustation 2 cigarette packets 1 are in the form of a Stack of equally oriented, adjacent and aligned Cigarette packs before.
- the barrier 6 projects into the stream of Cigarette packs 1 inside.
- the five-stack 9a in front of the barrier 6 forms the next to be marked stack of cigarette packs.
- the Clamping devices 10, 11 protrude into the stream of cigarette packs 1 in FIG. 1 into and fix the stack 9 currently in the marking station 3, so that the cigarette packs 1 are reliably marked with a secure hold can be.
- the downstream stack 9p in the separating station 4 stands for a separation ready.
- the transport device 8 is in the first position, out of engagement with the stacks 9, 9a. In this position are preferably three side surfaces of the cigarette packs 1 substantially freely accessible.
- Fig. 2 shows the device in a side view and in a plan view immediately before a transport of stacks 9, 9a.
- the transport device 8 is brought into the second position to the stack 9, 9a to capture, for example, laterally clamp. Furthermore, the lock 6 and the Clamping devices 10, 11 transferred to a second position in which these no longer to intervene in the flow of cigarette packets 1. As shown in Fig. 2, was in the meantime, the previously marked stack 9p is separated and transported away.
- a gap in the example shown a gap of about 3 to 4 Cigarette packs 1.
- To achieve the highest possible throughput of the system ensure the time required to transport, mark and Releasing the stack 9, 9a and for returning the transport device. 8 is needed, in about the time required for onward transport of a number of Cigarette packs 1 is needed, the by the onward transport corresponds to the resulting gap.
- the timing of the device is corresponding selected.
- the compact stack transferred to the identification station will be there characterized by, for example, labeling by means of an inkjet printer, Laser printer, laser ablation or similar procedures.
- the labeling can take place on all three exposed sides of the cigarette packs 1. She can on one, two or three pages, at one point or at another several places per page. The marking can be successively, individually depending Packing or by simultaneous labeling of all packs.
- the processing of the cigarette packs in the identification station takes place as Stack, which is in contrast to the known from the prior art packaged labeling.
- the identification device for example Printing device, and / or the stack 9 or can be stack and Move identification device relative to each other.
- the stack 9 can be fixed, including the transport device 8, in particular the lateral jaws shown in the figures, or the again in the stream of cigarette packs introduced clamping devices 10, 11 can be used.
- Fig. 4 shows the device immediately after returning to the Starting position shown in FIG. 1.
- the transport device For returning the transport device give the two lateral jaws 8, the stack 9, 9 a free, the Jaws 8 raised and upstream back to the starting position pulled as shown in FIG. Finally, the jaws 8 are vertical moved down. Further, the lock 6 and the clamping devices 10, 11 return back to the first position to enter the stream of cigarette packets 1 intervene.
- the clamping devices 10, 11 automatically clamp the from the defrost station 2 in the marking station 3 transferred stack 9a as a stack 9.
- the gap between the front end of the Stream of cigarette packs and the lock 6 not yet complete open minded. By further supplying cigarette packs 1, this is Gap finally unlocked, so that the state shown in FIG. 1 again is taken.
- the transport device is designed so that Both the stack 9a in the Mestaustation and the stack 9 in the Identification station can be detected, so that both stacks 9, 9a simultaneously can be transported on.
- the support surface 7 in the area of Identification station 3 is preferably immobile, especially as in Essentially flat bearing surface formed, wherein the transport of the stack 9, 9a in the illustrated device preferably exclusively by means of Transport device 8 takes place.
- the marking devices used may be laterally and / or can be located above the identification position and can in principle also be kept movable, only in the vicinity of the stack to be marked 9 to arrive when the stack is to be marked and / or fixed.
- the device according to the invention can be used in conventional Cigarette packaging units are integrated easily, in particular also as an autonomous unit working with the other components of a Packaging machine coordinates cooperates.
- Such an arrangement become the incoming into the device according to the invention cigarette packets by means of conventional conveying means, in particular belt conveyors, on the support surface 7 pushed where they are marked and after separating the other units be supplied to the packaging machine.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Wrapping Of Specific Fragile Articles (AREA)
- Radar Systems Or Details Thereof (AREA)
- Labeling Devices (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
Description
- Fig. 1
- eine Vorrichtung zum Kennzeichnen von Zigarettenpackungen gemäß der vorliegenden Erfindung in einer Ausgangsstellung jeweils in einer Seitenansicht und einer Draufsicht darstellt;
- Fig. 2
- die Vorrichtung gemäß Fig. 1 unmittelbar vor einem Transport von zwei Stapeln von Zigarettenpackungen jeweils in einer Seitenansicht und einer Draufsicht darstellt;
- Fig. 3
- die Vorrichtung gemäß Fig. 1 unmittelbar nach einem Transport von zwei Zigarettenpackungen jeweils in einer Seitenansicht und einer Draufsicht darstellt; und
- Fig. 4
- die Vorrichtung gemäß Fig. 1 kurz vor Erreichen der in Fig. 1 dargestellten Ausgangsstellung jeweils in einer Seitenansicht und einer Draufsicht darstellt.
Claims (12)
- Vorrichtung zum Kennzeichnen von Zigarettenpackungen (1)a) mit einer ersten Transportvorrichtung für die kontinuierliche Förderung eines Stromes von Zigarettenpackungen (1) aus einer Zigarettenverpackungsmaschine, gekennzeichnet durch die folgenden Merkmale:b) eine Aufstaustation (2) zur Bildung eines stillstehenden Stapels (9) von mit ihren Breitseiten aneinander liegenden, ausgerichteten Zigarettenpackungen (1) aus diesem Strom;c) eine zweite Transportvorrichtung für den Transport eines Stapels (9) von Zigarettenpackungen (1) in eine Kennzeichnungsstation (3) zur Beschriftung mindestens einer freiliegenden Fläche (18, 19);d) die zweite Transportvorrichtung (8) weist bewegbare Klemmbacken (8) zur gemeinsamen Erfassung und zur Freigabe von zwei aufeinander folgenden, ausgerichteten Stapeln (9, 9a) sowie motorische Verstellmittel für den gleichzeitigen Transport eines ersten Stapels (9a) aus der Aufstaustation (2) in die Kennzeichnungsstation (3) und eines zweiten Stapels (9) aus der Kennzeichnungsstation (3) zu einer nachgeordneten Vereinzelungsstation (4) auf; unde) die Kennzeichnungsstation (3) kennzeichnet die Zigarettenpackungen (1) des ersten Stapels (9) stapelweise auf mindestens einer ihrer freiliegenden Flächen (18, 19).
- Vorrichtung nach Anspruch 1, bei der in der Kennzeichnungsstation (3) zumindest eine Fläche (18, 19) und maximal drei Flächen einer Zigarettenverpackung (9) frei liegt/liegen.
- Vorrichtung nach einem der Ansprüche 1 oder 2, bei der in der Kennzeichnungsstation (3) die Klemmbacken (8) den ersten Stapel (9) freigeben oder zur Beschriftung fixieren.
- Vorrichtung nach einem der vorhergehenden Ansprüche, bei der die Kennzeichnung der Zigarettenpackungen (1) durch Bedrucken erfolgt, wobei eine Druckvorrichtung und/oder der Stapel (9) während des Bedruckens stationär ist, oder der Stapel (9) und eine Druckvorrichtung während des Bedruckens relativ zueinander bewegbar sind.
- Vorrichtung nach Anspruch 4, bei der die Druckvorrichtung zumindest eine Laservorrichtung zur Kennzeichnung von Zigarettenpackungen mittels Laserbeschriftung oder mittels Laserablation umfasst.
- Vorrichtung nach einem der vorhergehenden Ansprüche, bei der die Kennzeichnungsstation (3) vor oder hinter einer Cellophanierstation angeordnet ist und/oder gekennzeichnete Zigarettenpackungen nach der Kennzeichnung für eine Cellophanierung wieder vereinzelt werden, insbesondere gekennzeichnete, bereits cellophanierte Zigarettenpackungen als Fünferstapel zu einer Verpackungsvorrichtung transportiert werden, um dort zu Stangen abgepackt zu werden.
- Verfahren zum Kennzeichnen von Zigarettenpackungen (1),a) die von einer ersten Transportvorrichtung in einem kontinuierlichen Strom aus einer Zigarettenverpackungsmaschine abtransportiert und zu einem stillstehenden Stapel (9) von mit ihren Breitseiten aneinander liegenden, ausgerichteten Zigarettenpackungen (1) aufgestaut werden;b) eine zweite Transportvorrichtung (8) erfasst zwei aufeinander folgende, ausgerichtete aufgestaute Stapel (9, 9a) und bringt einen ersten Stapel (9) aus der Aufstaustation (2) in eine Kennzeichnungsstation (3) und gleichzeitig einen zweiten Stapel aus der Kennzeichnungsstation (3) zu einer nachgeordneten Vereinzelungsstation (4); undc) die Zigarettenpackungen werden in der Kennzeichnungsstation (3) stapelweise beschriftet.
- Verfahren nach Anspruch 7, bei dem in der Kennzeichnungsstation (3) zumindest eine Fläche (18, 19) und maximal drei Flächen einer Zigarettenpackung (1) freiliegen.
- Verfahren nach Anspruch 7, bei dem der erste Stapel (9a) in der Kennzeichnungsstation (3) freigegeben oder der erste Stapel (9) in der Kennzeichnungsstation (3) mittels Klemmbacken (8) der zweiten Transportvorrichtung (8) fixiert wird.
- Verfahren nach einem der Ansprüche 7 bis 9, bei dem die Kennzeichnung durch Bedrucken von Zigarettenpackungen erfolgt, wobei eine Druckvorrichtung und/oder der Stapel (9) während des Bedruckens stationär ist/sind und/oder der Stapel (9) und eine Druckvorrichtung während des Bedruckens relativ zueinander bewegt werden.
- Verfahren nach Anspruch 10, bei dem der Stapel (9) von Zigarettenpackungen mit zumindest einer Laservorrichtung in der Kennzeichnungsstation (3) bedruckt wird, insbesondere mit Laserablation.
- Verfahren nach einem der Ansprüche 7 bis 11, bei dem die Kennzeichnung vor oder hinter einer Cellophanierstation erfolgt und/oder gekennzeichnete Zigarettenpackungen (1) nach der Kennzeichnung zur Cellophanierung wieder vereinzelt werden, insbesondere gekennzeichnete, bereits cellophanierte Zigarettenpackungen als Fünferstapel zu einer Verpackungsvorrichtung transportiert werden, um dort zu Gebinden abgepackt zu werden.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10221837A DE10221837B4 (de) | 2002-05-16 | 2002-05-16 | Vorrichtung und Verfahren zum Kennzeichnen von Zigarettenpackungen |
| DE10221837 | 2002-05-16 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1362791A1 EP1362791A1 (de) | 2003-11-19 |
| EP1362791B1 true EP1362791B1 (de) | 2005-11-30 |
Family
ID=29265326
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP03004932A Expired - Lifetime EP1362791B1 (de) | 2002-05-16 | 2003-03-07 | Vorrichtung und Verfahren zum Kennzeichnen von Zigarettenpackungen |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US6857358B2 (de) |
| EP (1) | EP1362791B1 (de) |
| AT (1) | ATE311328T1 (de) |
| DE (2) | DE10221837B4 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103072806A (zh) * | 2013-01-23 | 2013-05-01 | 中国烟草总公司重庆市公司万州分公司 | 一种条烟打码姿态控制装置 |
Families Citing this family (47)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE202004008007U1 (de) * | 2004-05-18 | 2004-10-07 | Wolf, Hans | Durchlaufsiegelgerät |
| GB0718706D0 (en) | 2007-09-25 | 2007-11-07 | Creative Physics Ltd | Method and apparatus for reducing laser speckle |
| DE102006037109B4 (de) * | 2006-08-07 | 2010-11-11 | Kba-Metronic Aktiengesellschaft | Verfahren und Vorrichtung zur Bedruckung von Einzelobjekten |
| AT505463B1 (de) * | 2007-06-04 | 2009-05-15 | Durst Phototech Digital Tech | Verfahren zum bedrucken von plattenmaterial |
| EP2207684B1 (de) * | 2007-10-19 | 2011-11-23 | KHS GmbH | Vorrichtung zum bedrucken von flaschen oder dergleichen behältern an der behälteraussenfläche |
| DE102007054147A1 (de) * | 2007-11-12 | 2009-05-20 | Khs Ag | Leimwalze sowie Etikettieraggregat mit einer solchen Leimwalze |
| DE102008060846A1 (de) * | 2008-12-06 | 2010-06-10 | Krones Ag | Vorrichtung und Verfahren zum Gruppieren von Artikeln |
| US8522515B2 (en) * | 2009-01-26 | 2013-09-03 | R.J. Reynolds Tobacco Company | Method and apparatus for customizing cigarette packages |
| US11726332B2 (en) | 2009-04-27 | 2023-08-15 | Digilens Inc. | Diffractive projection apparatus |
| ITBO20090317A1 (it) * | 2009-05-15 | 2010-11-16 | Gd Spa | Macchina e metodo per l'impacchettamento di sigarette. |
| US9274349B2 (en) | 2011-04-07 | 2016-03-01 | Digilens Inc. | Laser despeckler based on angular diversity |
| US10670876B2 (en) | 2011-08-24 | 2020-06-02 | Digilens Inc. | Waveguide laser illuminator incorporating a despeckler |
| WO2016020630A2 (en) | 2014-08-08 | 2016-02-11 | Milan Momcilo Popovich | Waveguide laser illuminator incorporating a despeckler |
| WO2013163347A1 (en) | 2012-04-25 | 2013-10-31 | Rockwell Collins, Inc. | Holographic wide angle display |
| US9456744B2 (en) | 2012-05-11 | 2016-10-04 | Digilens, Inc. | Apparatus for eye tracking |
| US9933684B2 (en) | 2012-11-16 | 2018-04-03 | Rockwell Collins, Inc. | Transparent waveguide display providing upper and lower fields of view having a specific light output aperture configuration |
| WO2014188149A1 (en) | 2013-05-20 | 2014-11-27 | Milan Momcilo Popovich | Holographic waveguide eye tracker |
| GB2551414B (en) * | 2013-08-08 | 2018-03-07 | Packaging Automation Ltd | Improvements in and relating to packaging apparatus |
| GB2517145B (en) * | 2013-08-08 | 2017-04-26 | Packaging Automation Ltd | Improvements in and relating to packaging apparatus |
| US10241330B2 (en) | 2014-09-19 | 2019-03-26 | Digilens, Inc. | Method and apparatus for generating input images for holographic waveguide displays |
| EP3198192A1 (de) | 2014-09-26 | 2017-08-02 | Milan Momcilo Popovich | Optischer tracker mit holografischem wellenleiter |
| EP3245444B1 (de) | 2015-01-12 | 2021-09-08 | DigiLens Inc. | Umweltisolierte wellenleiteranzeige |
| WO2016113533A2 (en) | 2015-01-12 | 2016-07-21 | Milan Momcilo Popovich | Holographic waveguide light field displays |
| WO2016116733A1 (en) | 2015-01-20 | 2016-07-28 | Milan Momcilo Popovich | Holographic waveguide lidar |
| US9632226B2 (en) | 2015-02-12 | 2017-04-25 | Digilens Inc. | Waveguide grating device |
| PL3070013T3 (pl) * | 2015-03-17 | 2017-12-29 | Köhl Maschinenbau AG | Urządzenie kodujące do kodowania opakowań zbiorczych, sposób kodowania opakowania zbiorczego oraz system etykietujący z urządzeniem kodującym |
| CN113759555B (zh) | 2015-10-05 | 2024-09-20 | 迪吉伦斯公司 | 波导显示器 |
| US10983340B2 (en) | 2016-02-04 | 2021-04-20 | Digilens Inc. | Holographic waveguide optical tracker |
| CN107187920A (zh) * | 2016-03-15 | 2017-09-22 | 莫登芬 | 一种在生产设备上能将不同内容印刷品交叉叠放的装置 |
| EP3548939A4 (de) | 2016-12-02 | 2020-11-25 | DigiLens Inc. | Wellenleitervorrichtung mit gleichmässiger ausgabebeleuchtung |
| CN106428829A (zh) * | 2016-12-06 | 2017-02-22 | 山东丽鹏股份有限公司 | 异形塑料盖激光打码机 |
| WO2018129398A1 (en) | 2017-01-05 | 2018-07-12 | Digilens, Inc. | Wearable heads up displays |
| WO2018141772A1 (en) * | 2017-02-01 | 2018-08-09 | Hicof Ag | Method and coding line for serializing a plurality of products |
| KR20250004154A (ko) | 2018-01-08 | 2025-01-07 | 디지렌즈 인코포레이티드. | 광 도파관의 제조 방법 |
| US10732569B2 (en) | 2018-01-08 | 2020-08-04 | Digilens Inc. | Systems and methods for high-throughput recording of holographic gratings in waveguide cells |
| US20190212588A1 (en) | 2018-01-08 | 2019-07-11 | Digilens, Inc. | Systems and Methods for Manufacturing Waveguide Cells |
| WO2020149956A1 (en) | 2019-01-14 | 2020-07-23 | Digilens Inc. | Holographic waveguide display with light control layer |
| US20200247017A1 (en) | 2019-02-05 | 2020-08-06 | Digilens Inc. | Methods for Compensating for Optical Surface Nonuniformity |
| CN113692544B (zh) | 2019-02-15 | 2025-04-22 | 迪吉伦斯公司 | 使用集成光栅提供全息波导显示的方法和装置 |
| US20220283377A1 (en) | 2019-02-15 | 2022-09-08 | Digilens Inc. | Wide Angle Waveguide Display |
| CN114207492A (zh) | 2019-06-07 | 2022-03-18 | 迪吉伦斯公司 | 带透射光栅和反射光栅的波导及其生产方法 |
| US11681143B2 (en) | 2019-07-29 | 2023-06-20 | Digilens Inc. | Methods and apparatus for multiplying the image resolution and field-of-view of a pixelated display |
| KR102775783B1 (ko) | 2019-08-29 | 2025-02-28 | 디지렌즈 인코포레이티드. | 진공 격자 및 이의 제조 방법 |
| WO2022150841A1 (en) | 2021-01-07 | 2022-07-14 | Digilens Inc. | Grating structures for color waveguides |
| EP4288831A4 (de) | 2021-03-05 | 2025-01-15 | Digilens Inc. | Evakuierte periodische strukturen und herstellungsverfahren |
| IT202100016553A1 (it) | 2021-06-24 | 2022-12-24 | Ima Spa | Apparecchiatura e procedimento per applicare automaticamente elementi stampati su pacchetti di articoli da fumo |
| CN118323542A (zh) * | 2024-06-05 | 2024-07-12 | 浙江中烟工业有限责任公司 | 一种多规格件烟调头装置及控制方法 |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| IT1186635B (it) * | 1985-10-23 | 1987-12-04 | Gd Spa | Dispositivo per la realizzazione ed il controllo dell'involucro esterno di pacchetti in una macchina impacchettatrice di sigarette |
| GB8927534D0 (en) * | 1989-12-06 | 1990-02-07 | Molins Plc | Cigarette manufacture |
| IT1303992B1 (it) * | 1998-06-03 | 2001-03-02 | Gd Spa | Convogliatore di stabilizzazione di pacchetti di sigarette in uscitada una macchina impacchettatrice . |
| DE19914297A1 (de) * | 1999-03-29 | 2000-10-05 | Focke & Co | Verfahren und Einrichtung zur Steuerung einer (Zigaretten-)Fertigungs- und Verpackungsanlage |
| DE10003674A1 (de) * | 2000-01-28 | 2001-08-02 | Hauni Maschinenbau Ag | Verfahren und Anordnung zum Herstellen eines aus mehreren Verpackungskomponenten gebildeten Verpackungsbehälters |
| DE10004022A1 (de) * | 2000-01-31 | 2001-08-02 | Focke & Co | Verfahren und Vorrichtung zum Anbringen von Codierungen an (Zigaretten-)Packungen |
| IT1321318B1 (it) * | 2000-07-11 | 2004-01-08 | Gd Spa | Dispositivo di uscita per pacchetti di sigarette da una macchinaimpacchettatrice. |
-
2002
- 2002-05-16 DE DE10221837A patent/DE10221837B4/de not_active Expired - Fee Related
-
2003
- 2003-03-07 AT AT03004932T patent/ATE311328T1/de not_active IP Right Cessation
- 2003-03-07 EP EP03004932A patent/EP1362791B1/de not_active Expired - Lifetime
- 2003-03-07 DE DE50301783T patent/DE50301783D1/de not_active Expired - Lifetime
- 2003-05-15 US US10/438,387 patent/US6857358B2/en not_active Expired - Fee Related
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103072806A (zh) * | 2013-01-23 | 2013-05-01 | 中国烟草总公司重庆市公司万州分公司 | 一种条烟打码姿态控制装置 |
| CN103072806B (zh) * | 2013-01-23 | 2016-01-27 | 中国烟草总公司重庆市公司万州分公司 | 一种条烟打码姿态控制装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| DE10221837B4 (de) | 2005-10-20 |
| DE10221837A1 (de) | 2003-12-24 |
| DE50301783D1 (de) | 2006-01-05 |
| US20040079243A1 (en) | 2004-04-29 |
| US6857358B2 (en) | 2005-02-22 |
| ATE311328T1 (de) | 2005-12-15 |
| EP1362791A1 (de) | 2003-11-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE10221837A1 (de) | Vorrichtung und Verfahren zum Kennzeichnen von Zigarettenpackungen | |
| EP3445692B1 (de) | Verfahren und vorrichtung zum umgang mit in mindestens zwei parallelen reihen bewegten stückgütern | |
| DE19814141C2 (de) | Verfahren und Vorrichtung zum positionsgenauen Zuführen von flächenförmigen Gütern zu einem Bearbeitungsprozeß | |
| DE10022272B4 (de) | Vorrichtung zum Palettieren von Paketen | |
| EP3027543B1 (de) | Palettiervorrichtung für verpackungseinheiten | |
| EP2110348B1 (de) | Palettiereinrichtung sowie Verfahren zum Übergeben von Paketen von einer Annahmestation an einen Paketgreifer | |
| EP1452452B1 (de) | Verfahren und Vorrichtung zum Herstellen von (Zigaretten-) Packungen | |
| EP4132852A1 (de) | Verpackungsvorrichtung und verfahren zum verpacken von artikeln | |
| DE102017118928A1 (de) | Lagenbildungs- und Palettiermodul und Verfahren zum Gruppieren und Palettieren von Stückgütern | |
| EP0607626B1 (de) | Verfahren und Vorrichtung zur Handhabung von Zuschnitt-Stapeln mit Banderole | |
| EP0272543B1 (de) | Einsteckvorrichtung, insbesondere für Falzprodukte | |
| DE3239378C2 (de) | ||
| EP3770086A1 (de) | Verfahren und vorrichtung zum umgang mit in mindestens einer reihe hintereinander bewegten stückgütern | |
| EP1751002B1 (de) | Verfahren und einrichtung zur verpackung von flachen objekten | |
| EP3583056A1 (de) | Vorrichtung und verfahren zur flexiblen verteilung von verpackungen | |
| EP3623323B1 (de) | Verfahren und vorrichtung zur handhabung von stückgütern, artikeln und/oder gebinden | |
| DE102013106368B4 (de) | Vorrichtung und Verfahren zur Bildung von Verpackungen | |
| EP3458366B1 (de) | Verfahren und vorrichtung zum etikettieren von ersten verpackungen | |
| WO2015014514A1 (de) | Stapelvorrichtung und stapelverfahren | |
| DE102005045864B4 (de) | Verpackungsanlage und Verpackungsverfahren | |
| EP1871672B1 (de) | Verfahren und system zur behandlung flexibler beutel | |
| EP1669312B1 (de) | Vorrichtung zum on-line Weitertransport von flachen Gegenständen, die von einer zuführenden Vorrichtung auf einem Träger gestapelt werden | |
| EP3070013B1 (de) | Codiervorrichtung zum codieren von gebindepackungen, verfahren zum codieren einer gebindepackung und etikettiersystem mit einer codiervorrichtung | |
| DE202015104636U1 (de) | Handhabungsvorrichtung für Stückgut | |
| EP0336179B1 (de) | Vorrichtung zum Stapeln von Druckprodukten |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO |
|
| 17P | Request for examination filed |
Effective date: 20040503 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20040914 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT SE SI SK TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051130 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051130 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051130 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051130 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051130 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH Ref country code: CH Ref legal event code: EP Ref country code: CH Ref legal event code: NV Representative=s name: KIRKER & CIE SA |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20051201 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50301783 Country of ref document: DE Date of ref document: 20060105 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060228 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060228 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060228 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060307 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060313 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060331 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060331 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060601 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20060831 |
|
| BERE | Be: lapsed |
Owner name: BRITISH AMERICAN TOBACCO (GERMANY) G.M.B.H. Effective date: 20060331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051130 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20150319 Year of fee payment: 13 Ref country code: DE Payment date: 20150320 Year of fee payment: 13 Ref country code: CH Payment date: 20150319 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20150319 Year of fee payment: 13 Ref country code: GB Payment date: 20150319 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20150330 Year of fee payment: 13 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50301783 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20160401 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20160307 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20161130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160331 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161001 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160307 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160331 Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160401 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160307 |