EP1228255B1 - Verfahren zum herstellen eines warmbandes - Google Patents
Verfahren zum herstellen eines warmbandes Download PDFInfo
- Publication number
- EP1228255B1 EP1228255B1 EP00966035A EP00966035A EP1228255B1 EP 1228255 B1 EP1228255 B1 EP 1228255B1 EP 00966035 A EP00966035 A EP 00966035A EP 00966035 A EP00966035 A EP 00966035A EP 1228255 B1 EP1228255 B1 EP 1228255B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- temperature
- strand
- strip
- hot
- cold
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/041—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing involving a particular fabrication or treatment of ingot or slab
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B1/00—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations
- B21B1/46—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling metal immediately subsequent to continuous casting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/04—Continuous casting of metals, i.e. casting in indefinite lengths into open-ended moulds
- B22D11/041—Continuous casting of metals, i.e. casting in indefinite lengths into open-ended moulds for vertical casting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/12—Accessories for subsequent treating or working cast stock in situ
- B22D11/1213—Accessories for subsequent treating or working cast stock in situ for heating or insulating strands
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/16—Controlling or regulating processes or operations
- B22D11/22—Controlling or regulating processes or operations for cooling cast stock or mould
- B22D11/225—Controlling or regulating processes or operations for cooling cast stock or mould for secondary cooling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/0421—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the working steps
- C21D8/0426—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/004—Heating the product
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/0421—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the working steps
- C21D8/0436—Cold rolling
Definitions
- the invention relates to a method for producing a Hot strip, especially for making one for the Determine generation of a well deep-drawing cold strip Hot strip, from a low-carbon, low-alloy Steel in which thin slabs are produced by continuous casting in which the during the continuous casting from a Casting strand exiting a cooling section passes through and in which the cast strand itself or thin slabs separated from the strand in one Equalization oven must be reheated before going to Hot rolled hot rolled.
- the known method makes use of after casting the heat present in the strand Production of hot strip with an energy expenditure, which compared to other conventional methods of this Kind is diminished.
- the equalizing oven to be operated at very high temperatures. This high temperatures lead to premature Wear of the furnace, the maintenance of which is therefore achieved Energy savings.
- the high temperatures of the Compensating furnace are however in the prior art needed to the alloy components of the steel strand to bring or keep in solution, which in the course of the further process steps in the manufacture of the Hot strip or the cold strip made from it
- the formation of excretions, which cause the Formation of a certain structure of the finished hot or the cold strip produced from it is crucial influence.
- EP 0 686 702 A1 describes a modification of the known method above, in which the Surface temperature of the slab between the casting mold and the equalizing furnace sufficiently strong is lowered that a in the slab Structural transformation from austenite to ferrite / pearlite. It is also stated that those achieved Temperatures at a depth of 2 mm below the Slab surface preferably less than 600 ° C be.
- the slabs cooled in this way are in the equalization furnace to the high ones, usually in the equalizing furnace set temperatures warmed.
- To for the Reheating as little energy as possible must be known from EP 0 686 702 A1 Process the depth of cooling and the reason for it scheduled time reduced to a minimum so that the Temperature inside the slab when entering the Compensation furnace is as high as possible.
- the strand is after casting and before reheating and hot rolling cooled to below Ar1, preferably to less than Ar1-200 ° C.
- the object of the invention is one Procedures of the type mentioned in the course of Processing of low-alloy, low-carbon steels the required temperatures in the compensating furnace lower that the load on the furnace is reduced without that there is a loss in the quality of the hot strip produced or a cold strip made from it.
- a method for producing a hot strip in particular for producing a hot strip intended for producing a deep-drawing cold strip, in which a molten steel which (in mass%) C: ⁇ 0.07%, Si: ⁇ 0.5%, Mn: ⁇ 2.5%, Al: ⁇ 0.1%, N: ⁇ 0.01%, P: ⁇ 0.025, B: ⁇ 0.05, possibly up to a total of 0.35% Nb, Ti and V, and the balance contains iron and usual impurities, in which the molten steel is continuously discharged from a casting mold in one strand, in which the cast strand is passed through a cooling section immediately after emerging from the casting mold, in which the entire strand is cooled intensively at a cooling rate of at least 3 K / s to a temperature of A r1 ⁇ 25 K, at which the strand is cooled in air for at least 30 seconds following its intensive cooling, and on the strand itself or from the strand divided D nnbrammen are
- the emerging from the casting mold line of an intensive cooling at cooling rates of at least 3 K / s is exposed in accordance with, (the temperature at which the transformation of austenite into ferrite completed) wherein the strand below the A r1 cooled -Temperature the excretions required for the formation of the desired material properties of the hot strip are specifically induced in the area which is to be upstream of the compensating furnace. So much time is available during the subsequent cooling in air after the intensive cooling that the excretion processes have essentially expired when entering the compensating furnace. At the same time, the temperature in the strand is homogenized so that there is a uniform temperature distribution when entering the furnace.
- the furnace temperature can be limited to temperatures which are lower than the reheating temperatures required in the conventional procedure.
- the temperature of the compensating furnace to be maintained according to the invention is expediently in a range whose lower limit is determined by the A r3 temperature and whose upper limit is 1150 ° C.
- Hot strip a cold strip is generated, which after the Cold rolling is annealed in a continuous furnace.
- this Case preferably take place during all with the Generation of hot and cold strip connected to the Reheating of the following work steps none Elimination takes place more so that it no longer is necessary in the formation of excretions Bring involved alloy components in solution.
- a cold rolled strip which after cold rolling in a hood furnace is annealed, so should the temperature when heating the strand or thin slabs in the Compensating furnace are in the range from 1100 ° C to 1150 ° C.
- a heating temperature above 1100 ° C Al nitride in solution to an extent sufficient to create a desired "pancake" structure in the course of the hood annealing to create.
- an in accordance with the invention Tape produced in this way has a fine-grained structure, which is beneficial to the thermoforming ability of one the cold rolled strip produced affects.
- the result of the invention is thus a method for Which allows the temperature in the To reduce the compensation furnace so that its service life is increased and the economics of the process improved compared to the conventional approach is.
- a method according to the invention provides a product that is excellent for a Processing by deep drawing is suitable.
- the finished rolled hot strip having a thickness of 2 to 5 mm.
- a decrease in thickness ⁇ h > 15% should be achieved in the last pass of the rolling.
- the hot-rolled strip thus rolled has a particularly fine-grained structure, which further improves its deep-drawing ability.
- the "shape change ⁇ h " is understood to mean the ratio of the decrease in thickness during the last pass to the thickness of the strip when it enters the last rolling stand of the hot rolling mill. Accordingly, a hot strip has a thickness h 0 before the last stitch, for example. After the last stitch, the thickness of the tape is reduced to h 1 .
- the final rolling temperature at the end of hot rolling is preferably at least 20 ° C. above the A r3 temperature. If, however, after hot rolling a substantially ferritic microstructure of the hot strip are present, so the final rolling temperature is preferably at the completion of the hot rolling less than the A r1 -Temperature + 50 ° C.
- a further improvement in the microstructure of a cold strip produced from the hot strip produced according to the invention with regard to the deep-drawing properties can be achieved in that the overall change in shape ⁇ total achieved during the cold rolling of the hot strip is at least 60%.
- the "overall change in shape ⁇ tot" is understood here to mean the ratio of the decrease in thickness during cold rolling to the thickness of the unwrought strip as it enters the cold rolling stand.
- a hot strip produced according to the invention has a thickness h 0, for example after hot rolling. After cold rolling, the thickness of the strip is reduced to h 1 .
- the finished rolled hot strip should be Reel temperature of at least 650 ° C. By observing this minimum temperature, the Formation of excretions in the coiled hot strip promoted so that the recrystallization of the cold strip during the continuous annealing of excretions can run freely.
- a melt of a low carbon, low alloy Steel is made via a casting mold 1 to a between 20 and 70 mm thick steel strand S.
- the steel strand S is intensively cooled by cooling water, which is directed onto the steel strand S from cooling devices 2 arranged on both sides of the steel strand S, in the course of a “metallurgical length” LM.
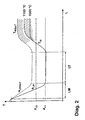
- the cooling rate a LM reached during the intense cooling of the steel strand S within the metallurgical length LM is at least 3 K / s, wherein the actually set cooling a LM depending on the thermal conductivity of the steel strand S and the required temperature T LM at the end of the metallurgical length LM is.
- the extent of the intensive cooling is in any case such that the steel strand S at the end of the metallurgical length LM has a temperature T LM of A r1 ⁇ 25 ° C, for example 710 ° C.
- T LM temperature of A r1 ⁇ 25 ° C, for example 710 ° C.
- the position of A is indicated r1 -Temperature depending on the carbon content of the composition of the steel strand S.
- a cooling section LT in which a cooling of the steel strand S in air he follows.
- the Steel strand S for at least 30 seconds, so that at the end of the Cooling section LT the formation of excretions in the Steel strand S is essentially complete and one homogeneous temperature distribution.
- the cooling section LT After run the cooling section LT occur, depending on the design of the Production line, the steel strand S itself or by him thin slabs divided by means of a compartment device 4 D in a compensating furnace 5.
- the steel strand S or the thin slabs D are heated to a reheating temperature T W , which is above the A r3 temperature, but below 1100 ° C.
- the location of the A r3 temperature is also in Diag. 1 depending on the carbon content of the steel composition.
- the temperature T W reached during the reheating in the equalizing furnace 5 depends on the annealing treatment which is carried out during the further processing of the hot strip produced from the steel strand S or the thin slabs D into cold strip. If the cold-rolled cold-rolled strip is subjected to a hood annealing, the reheating temperature T W is in the range of 1100 ° C. If, on the other hand, the cold strip passes through a continuous anneal, the reheating temperature T W is approx. 1000 ° C.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Heat Treatment Of Sheet Steel (AREA)
- Metal Rolling (AREA)
Description
- Fig. 1
- den Anfang einer Fertigungslinie zum Herstellen eines Warmbandes aus einem gegossenen Stahlstrang in seitlicher Ansicht;
- Diag. 1
- den Verlauf der Ar1- und Ar3-Temperaturen in Abhängigkeit vom Kohlenstoff-Gehalt eines kohlenstoffarmen Stahls;
- Diag. 2
- den Verlauf der Temperatur des Strangs im Bereich des in Fig. 1 dargestellten Anfangs einer Fertigungslinie.
- 1
- Gießkokille
- 2
- Kühleinrichtungen
- 3
- Rollgang
- 4
- Abteileinrichtung
- 5
- Ausgleichsofen
- D
- Dünnbrammen
- LM
- metallurgische Länge
- LT
- Abkühlstrecke
- L
- Wegachse des Diag. 2
- S
- Stahlstrang
- T
- Temperaturachse des Diag. 2
- TLM
- Temperatur am Ende der metallurgischen Länge LM
- TW
- Wiedererwärmungstemperatur
- TWStdT
- Wiedererwärmungstemperatur beim Stand der Technik
Claims (12)
- Verfahren zum Herstellen eines Warmbandes, insbesondere zum Herstellen eines für die Erzeugung eines gut tiefziehfähigen Kaltbandes bestimmten Warmbandes,bei dem eine Stahlschmelze, welche (in Masse-%)
C: ≤ 0,07 %
Si: ≤ 0,5 %
Mn: ≤ 2,5 %
Al: ≤ 0,1 %
N: ≤ 0,01 %
P: ≤ 0,025
B: ≤ 0,05
gegebenenfalls bis insgesamt 0,35 % an Nb, Ti und V, und
als Rest Eisen und übliche Verunreinigungen enthält, erschmolzen wird,bei dem die Stahlschmelze in einem Strang (S) kontinuierlich aus einer Gießkokille (1) ausgebracht wird,bei dem der gegossene Strang (S) unmittelbar nach dem Austritt aus der Gießkokille (1) durch eine Kühlstrecke (2) geleitet wird, in welcher der gesamte Strang (S) mit einer Abkühlrate (aLM) von mindestens 3 K/s auf eine Temperatur von Ar1 ± 25 K intensiv abgekühlt wird,bei dem der Strang (S) im Anschluß an seine intensive Abkühlung für mindestens 30 Sekunden an Luft gekühlt wird,bei dem der Strang (S) selbst oder von dem Strang (S) abgeteilte Dünnbrammen (D) in einem Ausgleichsofen (5) wiedererwärmt werden, bevor der Strang (S) oder die Dünnbrammen (D) zu Warmband warmgewalzt werden. - Verfahren nach Anspruch 1, dadurch gekennzeichnet, daß der Strang (S) oder die Dünnbrammen (D) in dem Ausgleichsofen (5) auf eine oberhalb der Ar3-Temperatur liegende, jedoch 1100 °C nicht überschreitende Temperatur (TW) wiedererwärmt werden.
- Verfahren nach einem der voranstehenden Ansprüche, dadurch gekennzeichnet, daß die Dicke der Dünnbrammen 20 - 70 mm beträgt.
- Verfahren nach einem der voranstehenden Ansprüche, dadurch gekennzeichnet, daß während des Warmwalzens mehrere Walzstiche durchgeführt werden und daß das fertig gewalzte Warmband eine Dicke von 2 bis 5 mm aufweist.
- Verfahren nach Anspruch 4, dadurch gekennzeichnet, daß im letzten Stich des Warmwalzens eine Dickenabnahme εh > 15 % erreicht wird.
- Verfahren nach einem der Ansprüche 4 oder 5, dadurch gekennzeichnet, daß die Endwalztemperatur bei Beendigung des Warmwalzens um mindestens 20 °C oberhalb der Ar3-Temperatur liegt.
- Verfahren nach einem der Ansprüche 4 oder 5, dadurch gekennzeichnet, daß die Endwalztemperatur bei Beendigung des Warmwalzens weniger als die Ar1-Temperatur + 50 °C beträgt.
- Verfahren nach einem der Ansprüche 4 bis 7, dadurch gekennzeichnet, daß aus dem Warmband ein Kaltband kaltgewalzt wird und daß die während des Kaltwalzens erreichte Gesamtformänderung εges mindestens 60 % beträgt.
- Verfahren nach einem der Ansprüche 4 bis 8, dadurch gekennzeichnet, daß das Kaltband in einem Durchlaufofen geglüht wird und daß die Temperatur bei der Erwärmung des Strangs (S) oder der Dünnbrammen (D) im Ausgleichsofen (5) 1050 °C nicht überschreitet.
- Verfahren nach Anspruch 9, dadurch gekennzeichnet, daß das fertig gewalzte Warmband bei einer Haspeltemperatur von mindestens 650 °C gehaspelt wird.
- Verfahren nach einem der Ansprüche 4 bis 8, dadurch gekennzeichnet, daß das Kaltband in einem Haubenofen geglüht wird und daß die Temperatur bei der Erwärmung des Strangs (S) oder der Dünnbrammen (D) im Ausgleichsofen (5) im Bereich von 1100 °C bis 1150 °C liegt.
- Verfahren nach Anspruch 11, dadurch gekennzeichnet, daß das fertig gewalzte Warmband bei einer Haspeltemperatur von höchstens 625 °C gehaspelt wird.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19950502 | 1999-10-20 | ||
| DE19950502A DE19950502C1 (de) | 1999-10-20 | 1999-10-20 | Verfahren zum Herstellen eines Warmbandes |
| PCT/EP2000/009063 WO2001029273A1 (de) | 1999-10-20 | 2000-09-16 | Verfahren zum herstellen eines warmbandes |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1228255A1 EP1228255A1 (de) | 2002-08-07 |
| EP1228255B1 true EP1228255B1 (de) | 2004-08-25 |
Family
ID=7926268
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP00966035A Expired - Lifetime EP1228255B1 (de) | 1999-10-20 | 2000-09-16 | Verfahren zum herstellen eines warmbandes |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US6835253B1 (de) |
| EP (1) | EP1228255B1 (de) |
| AU (1) | AU7657400A (de) |
| DE (2) | DE19950502C1 (de) |
| ES (1) | ES2223585T3 (de) |
| WO (1) | WO2001029273A1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110743911A (zh) * | 2019-10-24 | 2020-02-04 | 中铝瑞闽股份有限公司 | 一种钎焊板用铝合金卷的热轧复合方法 |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US8333923B2 (en) * | 2007-02-28 | 2012-12-18 | Caterpillar Inc. | High strength gray cast iron |
| US20090084517A1 (en) | 2007-05-07 | 2009-04-02 | Thomas Brian G | Cooling control system for continuous casting of metal |
| JP4678448B2 (ja) * | 2009-07-15 | 2011-04-27 | 住友金属工業株式会社 | 熱延鋼板の製造装置、及び鋼板の製造方法 |
| DE102014214374A1 (de) * | 2014-07-23 | 2016-01-28 | Sms Group Gmbh | Verfahren zur Herstellung eines metallischen Produkts |
| KR102361377B1 (ko) | 2017-06-27 | 2022-02-10 | 캐논 아네르바 가부시키가이샤 | 플라스마 처리 장치 |
| DE102020205655A1 (de) | 2020-05-05 | 2021-11-11 | Sms Group Gmbh | Verfahren zum Steuern oder Regeln der Temperatur eines Stahlbandes bei der Warmumformung in einer Warmbandstraße |
| CN115478221A (zh) * | 2022-09-20 | 2022-12-16 | 武汉钢铁有限公司 | 一种基于CSP工艺的450MPa级磁极钢及其制造方法 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5168422A (en) | 1974-12-11 | 1976-06-14 | Nippon Steel Corp | Kyojinkono seizoho |
| JPS6045689B2 (ja) | 1982-02-19 | 1985-10-11 | 川崎製鉄株式会社 | プレス成形性にすぐれた冷延鋼板の製造方法 |
| FR2544333B1 (fr) | 1983-04-18 | 1988-05-20 | Siderurgie Fse Inst Rech | Procede pour l'obtention de toles laminees a froid et recuites |
| DE3818879C1 (de) | 1988-06-01 | 1989-11-16 | Mannesmann Ag, 4000 Duesseldorf, De | |
| DE4416752A1 (de) * | 1994-05-13 | 1995-11-16 | Schloemann Siemag Ag | Verfahren und Produktionsanlage zur Erzeugung von Warmbreitband |
-
1999
- 1999-10-20 DE DE19950502A patent/DE19950502C1/de not_active Expired - Fee Related
-
2000
- 2000-09-16 DE DE50007566T patent/DE50007566D1/de not_active Expired - Lifetime
- 2000-09-16 ES ES00966035T patent/ES2223585T3/es not_active Expired - Lifetime
- 2000-09-16 EP EP00966035A patent/EP1228255B1/de not_active Expired - Lifetime
- 2000-09-16 AU AU76574/00A patent/AU7657400A/en not_active Abandoned
- 2000-09-16 WO PCT/EP2000/009063 patent/WO2001029273A1/de not_active Ceased
- 2000-09-16 US US10/111,119 patent/US6835253B1/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110743911A (zh) * | 2019-10-24 | 2020-02-04 | 中铝瑞闽股份有限公司 | 一种钎焊板用铝合金卷的热轧复合方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| ES2223585T3 (es) | 2005-03-01 |
| EP1228255A1 (de) | 2002-08-07 |
| WO2001029273A1 (de) | 2001-04-26 |
| DE50007566D1 (de) | 2004-09-30 |
| US6835253B1 (en) | 2004-12-28 |
| AU7657400A (en) | 2001-04-30 |
| DE19950502C1 (de) | 2000-11-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2663411B1 (de) | Verfahren zum herstellen eines warmgewalzten stahlflachprodukts | |
| EP1469954B2 (de) | Verfahren zur herstellung von warmband aus austenitischen nichtrostenden stählen | |
| DE19745445C1 (de) | Verfahren zur Herstellung von kornorientiertem Elektroblech mit geringem Ummagnetisierungsverlust und hoher Polarisation | |
| EP1752548B1 (de) | Verfahren zur Herstellung von kornorientiertem Elektroband | |
| EP1752549B1 (de) | Verfahren zur Herstellung von kornorientiertem Elektroband | |
| EP1305122B1 (de) | Produktionsverfahren und -anlage zur erzeugung von dünnen flachprodukten | |
| EP2855718B1 (de) | Stahlflachprodukt und verfahren zur herstellung eines stahlflachprodukts | |
| DE3825634C2 (de) | Verfahren zur Erzeugung von Warmbad oder Grobblechen | |
| DE60315129T2 (de) | Verfahren zur herstellung eines eisenhüttenprodukts aus unlegiertem stahl mit hohem kupfergehalt und danach erhaltenes eisenhüttenprodukt | |
| DE19936151A1 (de) | Höherfestes Stahlband oder -blech und Verfahren zu seiner Herstellung | |
| EP1319091B1 (de) | Verfahren zum herstellen eines überwiegend aus mn-austenit bestehenden stahlbands oder -blechs | |
| DE60207591T2 (de) | Verfahren zur herstellung von geschweissten röhren und dadurch hergestelltes rohr | |
| WO2018036918A1 (de) | Verfahren zur herstellung eines höchstfesten stahlbandes mit verbesserten eigenschaften bei der weiterverarbeitung und ein derartiges stahlband | |
| DE112020004399T5 (de) | Nb-mikrolegierter Stahl mit hoher Festigkeit und hohem Lochaufweitungsvermögen und Herstellungsverfahren dafür | |
| DE112020004425T5 (de) | Dünner hochkorrosionsbeständiger stahl und herstellungsverfahren dafür | |
| DE112020004433T5 (de) | Warmgewalztes Stahlblech/-band mit Beständigkeit gegen Schwefelsäure-Taupunktkorrosion und Herstellungsverfahren dafür | |
| EP2690184A1 (de) | Kaltgewalztes Stahlflachprodukt und Verfahren zu seiner Herstellung | |
| DE19950502C1 (de) | Verfahren zum Herstellen eines Warmbandes | |
| EP1319725B1 (de) | Verfahren zum Herstellen von Warmband | |
| EP2334830B1 (de) | Verfahren zur herstellung von warmband-walzgut aus siliziumstahl | |
| DE102020214427A1 (de) | Verfahren zum Herstellen eines Warmbandes mittels einer Gießwalzanlage | |
| DE3116419C2 (de) | Verfahren zur Herstellung eines kornorientierten, elektromagnetischen Siliciumstahlbandes | |
| EP1396549A1 (de) | Verfahren zum Herstellen eines perlitfreien warmgewalzten Stahlbands und nach diesem Verfahren hergestelltes Warmband | |
| DE2316324C2 (de) | Verfahren zum Herstellen von alterungsbeständigem Stahlblech | |
| EP1038978B1 (de) | Verfahren zum Herstellen eines Warmbandes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20020322 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| RTI1 | Title (correction) |
Free format text: METHOD FOR PRODUCING A HOT STRIP |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB NL |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50007566 Country of ref document: DE Date of ref document: 20040930 Kind code of ref document: P |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20040825 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2223585 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20050526 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20130918 Year of fee payment: 14 Ref country code: NL Payment date: 20130916 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20130918 Year of fee payment: 14 Ref country code: FR Payment date: 20130918 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20130918 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50007566 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20140916 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50007566 Country of ref document: DE Effective date: 20150401 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20150529 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150401 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140916 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140930 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20151029 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140917 |