EP0851830B1 - Verfahren zur herstellung von flossenpackungen und trenneinrichtung zur durchführung des verfahrens - Google Patents
Verfahren zur herstellung von flossenpackungen und trenneinrichtung zur durchführung des verfahrens Download PDFInfo
- Publication number
- EP0851830B1 EP0851830B1 EP96929164A EP96929164A EP0851830B1 EP 0851830 B1 EP0851830 B1 EP 0851830B1 EP 96929164 A EP96929164 A EP 96929164A EP 96929164 A EP96929164 A EP 96929164A EP 0851830 B1 EP0851830 B1 EP 0851830B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- tube
- crush
- crosswise
- edge
- corners
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 6
- 238000007789 sealing Methods 0.000 claims abstract description 15
- 238000004806 packaging method and process Methods 0.000 claims description 4
- 238000004519 manufacturing process Methods 0.000 description 1
- 230000035515 penetration Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F1/00—Perforating; Punching; Cutting-out; Stamping-out; Apparatus therefor
- B26F1/18—Perforating by slitting, i.e. forming cuts closed at their ends without removal of material
- B26F1/20—Perforating by slitting, i.e. forming cuts closed at their ends without removal of material with tools carried by a rotating drum or similar support
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D1/00—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor
- B26D1/0006—Cutting members therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D1/00—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor
- B26D1/01—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor involving a cutting member which does not travel with the work
- B26D1/12—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor involving a cutting member which does not travel with the work having a cutting member moving about an axis
- B26D1/25—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor involving a cutting member which does not travel with the work having a cutting member moving about an axis with a non-circular cutting member
- B26D1/34—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor involving a cutting member which does not travel with the work having a cutting member moving about an axis with a non-circular cutting member moving about an axis parallel to the line of cut
- B26D1/40—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor involving a cutting member which does not travel with the work having a cutting member moving about an axis with a non-circular cutting member moving about an axis parallel to the line of cut and coacting with a rotary member
- B26D1/405—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor involving a cutting member which does not travel with the work having a cutting member moving about an axis with a non-circular cutting member moving about an axis parallel to the line of cut and coacting with a rotary member for thin material, e.g. for sheets, strips or the like
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D3/00—Cutting work characterised by the nature of the cut made; Apparatus therefor
- B26D3/10—Making cuts of other than simple rectilinear form
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B51/00—Devices for, or methods of, sealing or securing package folds or closures; Devices for gathering or twisting wrappers, or necks of bags
- B65B51/10—Applying or generating heat or pressure or combinations thereof
- B65B51/26—Devices specially adapted for producing transverse or longitudinal seams in webs or tubes
- B65B51/30—Devices, e.g. jaws, for applying pressure and heat, e.g. for subdividing filled tubes
- B65B51/306—Counter-rotating devices
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
- B65B61/04—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for severing webs, or for separating joined packages
- B65B61/06—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for severing webs, or for separating joined packages by cutting
- B65B61/08—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for severing webs, or for separating joined packages by cutting using rotary cutters
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D1/00—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor
- B26D1/0006—Cutting members therefor
- B26D2001/0053—Cutting members therefor having a special cutting edge section or blade section
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D1/00—Cutting through work characterised by the nature or movement of the cutting member or particular materials not otherwise provided for; Apparatus or machines therefor; Cutting members therefor
- B26D1/0006—Cutting members therefor
- B26D2001/006—Cutting members therefor the cutting blade having a special shape, e.g. a special outline, serrations
Definitions
- EP-A-659 645 describes a method and an apparatus for Cross sealing and cutting a packaging tube according to Preamble of claims 1 and 3 known.
- the device has two circumferential cross sealing jaws, which a tubular film in Single bag divided and at the same time with a zigzag knife separates the individual bags from each other.
- the knife is in one built-in sealing jaw, while the other a counterholder contains.
- the zigzag cut should make it easier to tear open.
- it has been shown that an easy one Tear open by the consumer only with a very sharp knife is possible.
- the knife must be sharpened accordingly frequently become.
- the present invention is based on the object Eliminate disadvantage. This task is accomplished through the combination of features of claims solved.
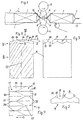
- Figure 1 is a cross sealing device for a packaging machine shown.
- One with a longitudinal seal 1 The formed film tube 3 contains at regular intervals the products to be packaged 2 and is in the conveying direction 4 funded.
- Parallel shafts 5, 6 are a sealing jaw 7 or a counter jaw 8 attached. Which contains a jaw 7 a squeeze knife 9, the other a counterholder 10.
- Das Crushing knife 9 cuts through the jaws 7, 8 formed Cross seal seam in the middle.
- the jaws 7, 8 the tube 3 initially at a first point 11. The cut is then made and then the cross seal on a second one Digit 12.
- the separated finished pack is with a Conveyor belt 13 removed.
- the crushing knife 9 is shown enlarged in FIGS. It has a zigzag crimp edge 16, which is formed by the penetration of V-shaped grooves 17, 18.
- the grooves leading in the direction 19 17 are compared to the trailing grooves 18 by half Groove width offset.
- the flanks 20, 21 of the grooves 17, 18 are flat and laterally shifted mirror-symmetrically to Middle plane 22 of the knife 9.
- the pinch edge 16 forms hence a plane 23.
- Two adjacent flanks 20, 21 lying side by side Grooves 17 and 18 form a leading Notch edge 24 or a trailing notch edge 25.
- Die Notched edges 24, 25 intersect the plane 23 under a pointed one Winel ⁇ of less than 50 °, preferably about 20 ° at leading corners 26 or trailing corners 27 of the Crimped edge 16.
- the grooves 17, 18 are arc-shaped.
- the bottom of the groove therefore has a radius r 1 and the notch edges 24, 25 have a radius r 2 .
- the flanks 20, 21 are frustoconical segment surfaces. This has the advantage that the grooves 17, 18 can be produced very efficiently on a cylindrical grinding machine.
- the embodiment according to FIGS. 8 and 9 differs from that according to FIGS. 6 and 7 in that the flanks 20, 21 are convexly curved with radii r 3 , r 4 in the end view according to FIG. 9, which are preferably the same.
- the flanks 20, 21 are therefore toroidal. This has the advantage that the pinch edge 16 no longer lies in one plane, but on a cylindrical surface, which is preferably coaxial to the shaft 5. This enables a more even cut to be achieved.
- the angle ⁇ is measured with respect to the tangent 31 to the cylindrical surface of the pinched edge 16 at the corner 27.
- the flanks 20, 21 can also be curved and straight Parts exist, such as with the dashed lines Lines in Fig. 9 is indicated.
- the flattening of the Pinch edge 16 can be within the plane 23 or Cylinder surface have a variable width.
- the notch edges 24, 25 are to be formed with sharp edges. This is achieved in that the same notch edge 24, 25 flanks 20, 21 ground one after the other become.
- Figure 10 shows a section of one described with Device manufactured tubular bag fin pack 35 with a transverse sealing seam 36 and a zigzag-shaped Cross-cut 37. From the concave sharp corners 38 of the cut 37 can in the longitudinal direction 39 of the pack 35 running notch cuts 40, which the slight tearing open of the pack by the consumer facilitate.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Life Sciences & Earth Sciences (AREA)
- Forests & Forestry (AREA)
- Packages (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
- Supplying Of Containers To The Packaging Station (AREA)
- Bag Frames (AREA)
Abstract
Description
- Figur 1
- eine schematische Seitenansicht einer Quersiegelvorrichtung,
- Figur 2
- einen Querschnitt durch ein Quetschmesser,
- Figuren 3 - 5
- Ansichten in Richtung der Pfeile III, IV und V in Fig. 2,
- Figuren 6 und 8
- Querschnitte durch zwei andere Ausführungsformen,
- Figuren 7 und 9
- Ansichten in Richtung der Pfeile VII bzw. IX in Figuren 6 bzw. 8, und
- Figur 10
- Ein Ausschnitt einer Packung.
Claims (10)
- Verfahren zur Herstellung von Flossenpackungen aus einem Schlauch (3) mit einer Längssiegelnaht (1) und Produkten (2), wobei der Schlauch (3) zwischen zwei gegenläufig umlaufenden Mitteln (7, 8) während der Umlaufbewegung an einer ersten Stelle (11) querversiegelt, dann zick-zack-förmig quergeschnitten und schliesslich an einer zweiten Stelle (12) querversiegelt wird, dadurch gekennzeichnet, dass nach der ersten Querversiegelung und vor dem Trennschnitt der Schlauch (3) anschliessend an die konkaven Ecken des Trennschnittes scharfkantig gekerbt wird.
- Verfahren nach Anspruch 1, wobei vor der zweiten Querversiegelung der Schlauch (3) nochmals scharfkantig gekerbt wird.
- Trenneinrichtung für eine SchlauchbeutelVerpackungsmaschine, umfassend eine umlaufende Siegelbacke (7) und eine Gegenbacke (8), wobei eine dieser Backen (7, 8) ein Messer (9) enthält, um zwischen einer ersten und einer zweiten Siegelstelle (11, 12) den Verpackungsschlauch (3) aufreissbar abzutrennen, dadurch gekennzeichnet, dass das Messer als Quetschmesser (9) ausgebildet ist, welches eine quer und längs zur Schlauchförderrichtung (4) angeordnete, mehrere Ecken (26, 27) aufweisende Quetschkante (16) aufweist, an deren vorlaufenden Ecken (26) je eine scharfe Kerbkante (24) parallel zur Schlauchförderrichtung (4) anschliesst, welche zur Tangente (23, 31) der durch die Quetschkante (16) definierten Fläche bei diesen vorlaufenden Ecken (26) einen Winkel (α) bildet.
- Einrichtung nach Anspruch 3, wobei an die nachlaufenden Ecken (27) der Quetschkante (16) weitere Kerbkanten (25) parallel zur Schlauchförderrichtung (4) in einem Winkel (α) zur dortigen Tangente (23, 31) zur Fläche der Quetschkante (16) anschliessen.
- Einrichtung nach Anspruch 4, wobei die vor- und nachlaufenden Kerbkanten (24, 25) gleiche Winkel (α) mit den betreffenden Tangenten (23) einschliessen.
- Einrichtung nach einem der Ansprüche 3 bis 5, wobei die Kerbkanten (24, 25) durch V-förmige Nuten (17, 18) gebildet sind, deren Flanken (20, 21) miteinander einen stumpfen Winkel (β) von vorzugsweise 95-150°, insbesondere etwa 120°, bilden.
- Einrichtung nach Anspruch 6, wobei die Flanken (20, 21) eine Kegelstumptsegment-Oberfläche bilden.
- Einrichtung nach Anspruch 6, wobei die Flanken (21, 21) im Querschnitt konvex gekrümmt sind.
- Einrichtung nach einem der Ansprüche 3 bis 8, wobei die Quetschkante (16) eine Abflachung von vorzugsweise 0,01-0,1mm Breite aufweist.
- Nach dem Verfahren gemäss Anspruch 1 oder 2 hergestellte Schlauchbeutel-Flossenpackung (35) mit zick-zack-förmigen Quer-Trennschnitten (37) benachbart einer Quersiegelnaht (36) dadurch gekennzeichnet, dass von den konkaven Ecken (38) der Trennschnitte (37) der Packung (35) scharfe Kerbungen (40) ausgehen.
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CH2690/95 | 1995-09-22 | ||
| CH269095 | 1995-09-22 | ||
| CH269095 | 1995-09-22 | ||
| PCT/CH1996/000324 WO1997010996A1 (de) | 1995-09-22 | 1996-09-19 | Verfahren zur herstellung von flossenpackungen und trenneinrichtung zur durchführung des verfahrens |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0851830A1 EP0851830A1 (de) | 1998-07-08 |
| EP0851830B1 true EP0851830B1 (de) | 2000-01-05 |
Family
ID=4239390
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP96929164A Expired - Lifetime EP0851830B1 (de) | 1995-09-22 | 1996-09-19 | Verfahren zur herstellung von flossenpackungen und trenneinrichtung zur durchführung des verfahrens |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US6023917A (de) |
| EP (1) | EP0851830B1 (de) |
| AU (1) | AU6868596A (de) |
| DE (1) | DE59604129D1 (de) |
| ES (1) | ES2142085T3 (de) |
| WO (1) | WO1997010996A1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US8473017B2 (en) | 2005-10-14 | 2013-06-25 | Pulse Finland Oy | Adjustable antenna and methods |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| NL1020191C2 (nl) * | 2002-03-18 | 2003-09-19 | Cortech Protect B V | Lemmet, werkwijze voor het snijden met het lemmet, en verpakkingsinrichting. |
| AU2005270662B2 (en) * | 2004-08-13 | 2009-05-28 | Kencan Australasia Pty Ltd | Method and apparatus for forming and filling flexible packaging |
| EP1786672A2 (de) | 2004-08-13 | 2007-05-23 | Kencan Australasia Pty Ltd | Verfahren und vorrichtung zur bildung und füllung einer verpackung |
| US10350776B2 (en) * | 2016-05-11 | 2019-07-16 | Zenith Cutter, Inc. | Cutoff knife serration |
| US11618177B1 (en) | 2022-04-12 | 2023-04-04 | Bradley W Boesel | Orbital knife |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH507786A (de) * | 1969-05-06 | 1971-05-31 | Sig Schweiz Industrieges | Schneidvorrichtung mit rotierendem Zick-Zack-Messer |
| US3943686A (en) * | 1974-09-05 | 1976-03-16 | Fmc Corporation | Wrapping machine with severing blade in crimping head |
| US4254601A (en) * | 1979-02-23 | 1981-03-10 | Keebler Company | Packaging machine having a slitter for forming slits in ends of packages |
| EP0055211B1 (de) * | 1980-12-24 | 1984-09-05 | SIG Schweizerische Industrie-Gesellschaft | Siegelbackenanordnung |
| US4582555A (en) * | 1984-12-17 | 1986-04-15 | Crown Zellerbach Corporation | Heatseal die |
| US4949846A (en) * | 1989-07-31 | 1990-08-21 | Lakey Lawrence D | Package end sealing and cutting method and apparatus |
| US5456055A (en) * | 1993-09-24 | 1995-10-10 | Johnson & Johnson, Inc. | Package for dispensing a fluid treating substance and method and apparatus for heat-sealing the dispensing package |
| US5477656A (en) * | 1993-12-21 | 1995-12-26 | Sig Schweizerische Industrie-Gesellschaft | Apparatus for making groups of interconnected bag packages |
-
1996
- 1996-09-19 DE DE59604129T patent/DE59604129D1/de not_active Expired - Lifetime
- 1996-09-19 US US09/043,173 patent/US6023917A/en not_active Expired - Lifetime
- 1996-09-19 WO PCT/CH1996/000324 patent/WO1997010996A1/de not_active Ceased
- 1996-09-19 ES ES96929164T patent/ES2142085T3/es not_active Expired - Lifetime
- 1996-09-19 EP EP96929164A patent/EP0851830B1/de not_active Expired - Lifetime
- 1996-09-19 AU AU68685/96A patent/AU6868596A/en not_active Abandoned
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US8473017B2 (en) | 2005-10-14 | 2013-06-25 | Pulse Finland Oy | Adjustable antenna and methods |
Also Published As
| Publication number | Publication date |
|---|---|
| ES2142085T3 (es) | 2000-04-01 |
| EP0851830A1 (de) | 1998-07-08 |
| WO1997010996A1 (de) | 1997-03-27 |
| US6023917A (en) | 2000-02-15 |
| AU6868596A (en) | 1997-04-09 |
| DE59604129D1 (de) | 2000-02-10 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69716390T2 (de) | Vorrichtung und Verfahren zur Herstellung von Handgriffen in Kunststoffbeuteln | |
| DE3814448C2 (de) | ||
| EP3718715B1 (de) | Längsschneidung mit integrierter förderrolle | |
| DE3324366C2 (de) | Vorrichtung zum Abtrennen von Umhüllungstreifen von einem Band für die Verbindung von Filter und Zigarette | |
| DE69602675T2 (de) | Wärmeschweissvorrichtung | |
| DE68908306T2 (de) | Verfahren und Vorrichtung zum Herstellen eines laminierten Streifens. | |
| DE60027421T2 (de) | Vorrichtung zum verformen und heissiegeln von behältern | |
| DE602005005806T2 (de) | Rotationseinheit zur ultraschalldichtung von röhrenförmigen endlosbändern | |
| EP0659645B1 (de) | Vorrichtung zum Herstellen von in Gruppen zusammenhängenden Schlauchbeutel-Packungen | |
| EP0367016B1 (de) | Vorrichtung zum Aufbereiten von unvulkanisierten Kautschuk | |
| DE69704088T2 (de) | Spannband mit ineinandergreifenden Enden | |
| DE3226879C2 (de) | ||
| EP2387495B1 (de) | VORRICHTUNG ZUM SCHWEIßEN UND TRENNEN VON PACKSTOFFEN | |
| EP0813954A1 (de) | Verfahren und Vorrichtung zum Herstellen einer Polsterpackung und damit hergestellte Polsterpackung | |
| DE4338561A1 (de) | Vorrichtung zur Vorbereitung/Vorbehandlung verpreßbarer Hohlkörper für Recycling | |
| DE7338607U (de) | Vorrichtung zum zufuehren eines folienstreifens o.dgl. in zickzackform | |
| EP0851830A1 (de) | Verfahren zur herstellung von flossenpackungen und trenneinrichtung zur durchführung des verfahrens | |
| DE19505882B4 (de) | Vorrichtung zur Herstellung einer Kombination aus zwei zusammenhängenden Beuteln | |
| EP3319881B1 (de) | Verpackungsmaschine mit reststreifenentsorgung | |
| EP3126120B1 (de) | Verfahren und vorrichtung zur herstellung von säcken aus einem gewebeschlauch | |
| WO2020120579A1 (de) | Vorrichtung mit guillotine-ablängvorrichtung zum fertigen eines verpackungsmaterialerzeugnisses aus einem faserausgangsmaterial und verfahren zum fertigen eines verpackungsmaterialerzeugnisses | |
| EP0781189B1 (de) | Vorrichtung zum trennen von fliessmittelpackungen | |
| DE19549740B4 (de) | Vorrichtung zur Herstellung einer Kombination aus zwei zusammenhängenden Beuteln | |
| EP0255014B1 (de) | Verfahren zum kontinuierlichen Überlappungsverschweissen von grossflächigen Kunststoff-Folien oder -Platten | |
| EP0410226B1 (de) | Vorrichtung zum klebstofffreien Verbinden von Lagen aus Papier, dünnem Karton od. dgl. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19980323 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES GB IT NL |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SIG PACK SYSTEMS AG |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 19990407 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES GB IT NL |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20000106 |
|
| REF | Corresponds to: |
Ref document number: 59604129 Country of ref document: DE Date of ref document: 20000210 |
|
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2142085 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20110923 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20110928 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20120920 Year of fee payment: 17 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20120925 Year of fee payment: 17 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20121122 Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20130401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130401 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20131018 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120920 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20130919 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59604129 Country of ref document: DE Effective date: 20140401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130919 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130919 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140401 |