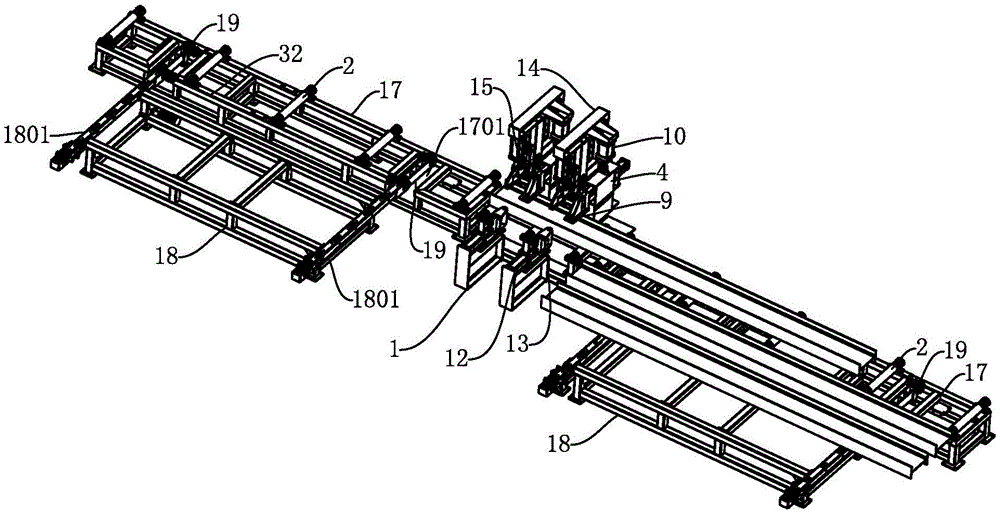
Parking equipment crossbeam and curb plate welding production line
Technical Field
The utility model belongs to the technical field of stereo garage production facility, especially, relate to a parking equipment crossbeam and curb plate welding production line.
Background
As shown in fig. 1, the side of the cross beam 100 of the parking equipment needs to be welded with the side plate 200 for connecting the longitudinal beams, then spraying treatment is carried out, processing needs to be completed on a welding production line, the cross beam 100 needs to be lifted to a feed roll of a welding and welding rack by using a crane, after the side plate is welded, the cross beam 100 is lifted to the next process by using the crane, time and labor are wasted, the labor intensity of an operator is high, the production efficiency is low, and the batch production requirement of the cross beam 100 cannot be met.
Therefore, in stereo garage production facility technical field, still there is research and modified demand to parking equipment crossbeam and curb plate welding production line, this is also a research focus and focus in present stereo garage production facility technical field, more the utility model discloses the starting point that can accomplish.
SUMMERY OF THE UTILITY MODEL
Therefore, the utility model discloses the technical problem that solve is: the utility model provides a parking equipment crossbeam and curb plate welding production line has improved crossbeam and curb plate butt joint efficiency, and then has improved the machining efficiency of crossbeam.
In order to solve the technical problem, the technical scheme of the utility model is that: a welding production line for a cross beam and a side plate of parking equipment comprises a welding rack, wherein material roller racks are arranged at two ends of the welding rack, a conveying frame is arranged on one side of the material roller frame, a plurality of feeding rollers are rotatably arranged on the welding frame and the material roller frame, a vertical bracket is arranged at one side of the welding rack, a material pushing box is vertically and slidably arranged on the vertical bracket, a plate containing box is fixedly arranged below the material pushing box and is communicated with the material pushing box, the bottom of the plate accommodating box is provided with a supporting plate driven by a first cylinder, the supporting plate is vertically and slidably arranged in the plate accommodating box, a push plate driven by a second cylinder is transversely installed in the material pushing box in a sliding manner, the sliding direction of the push plate is vertical to that of the supporting plate, the material pushing box is connected with the third cylinder, and a welding device is arranged on the welding rack and located at the position corresponding to the push plate.
As an improvement, one end of the push plate is provided with a convex edge used for pushing and blocking the side plate.
As a further improvement, a magnet for adsorbing the side plate is embedded on the push plate.
As a further improvement, one side of the welding rack is provided with a positioning roller for limiting the degree of freedom of the beam in the direction horizontally vertical to the conveying direction, the other side of the welding rack is provided with a sliding roller, the sliding roller is arranged in parallel with the positioning roller, and the sliding direction of the sliding roller is horizontally vertical to the conveying direction of the feeding roller.
As a further improvement, the sliding roller is connected with a fourth air cylinder.
As a further improvement, a connecting arm is fixedly mounted on the vertical support, and a pressing plate which is driven by a fifth cylinder and is used for pressing the cross beam is mounted on the connecting arm.
As a further improvement, be equipped with two piece at least parallel arrangement's delivery beam in the delivery frame, the swing arm is installed through the articulated shaft rotation to the head end of every delivery beam, the tip of swing arm rotates the first sprocket of installing connection power device, the tail end of delivery beam rotates installs the second sprocket, it has the conveying chain to encircle between first sprocket and the second sprocket, lie in the material roller frame delivery frame one side corresponds the swing arm position is equipped with the breach, the swing arm stretches into the breach just is located between two adjacent feed rolls, elevating system is connected to the swing arm.
As a further improvement, the lifting mechanism comprises a sixth air cylinder, the cylinder body of the sixth air cylinder is hinged and installed at a fixed position, the swing arm is hinged and provided with a connecting lug, and the piston rod of the sixth air cylinder is hinged and connected with the connecting lug.
As a further improvement, the hinged shafts of two adjacent conveying beams are connected through a transmission shaft.
As a further improvement, the power device comprises an electric motor in transmission connection with the transmission shaft, and the transmission shaft is in transmission connection with the first chain wheel.
After the technical scheme is adopted, the beneficial effects of the utility model are that:
the utility model provides a parking equipment crossbeam and curb plate welding production line, first cylinder drive layer board shifts up, and after the curb plate that is located the superiors runs into the push pedal that is in initial condition, the piston rod of second cylinder stretches out, drives the push pedal and with the welding position on a curb plate propelling movement to the crossbeam in the top, realizes the butt joint with curb plate and crossbeam, and the position is accurate, and the continuity is strong, and the butt joint is efficient, has improved the machining efficiency of crossbeam greatly.
Because the pressure plate used for compressing the cross beam is fixedly installed on the connecting arm, the degree of freedom of the vertical direction of the cross beam can be limited, and the stability of the cross beam and the side plate during welding can be ensured.
Owing to set up the swing arm of being connected with elevating system, the swing arm stretches into the breach and is located between two adjacent feed rolls, when needs shift the crossbeam to the material roller frame or shift to the transport frame from the material roller frame from the transport frame, elevating system lifting swing arm, the crossbeam can reach the delivery position of feed roll by the conveying chain through the swing arm, then elevating system drives the swing arm whereabouts, place the crossbeam on the feed roll, or lift the crossbeam on the feed roll through the swing arm, leave the feed roll, carry away from the feed roll by the conveying chain, avoided the crossbeam to drag on the feed roll, can not rub and damage the feed roll.
Because the motor is connected with the transmission shaft in a transmission way, and the transmission shaft is connected with the first chain wheel in a transmission way, the power transmission of the first chain wheel can be ensured, the swing arm can swing freely without influencing the power transmission, the structure is ingenious, and the use is flexible and reliable.
Because the articulated shaft passes through the transmission shaft rigid connection, consequently, the conveying chain only need a set of motor transmission can to simplified the structure, can enough guarantee the synchronization of conveying chain, reduced the use of power again, the cost is reduced.
Drawings
In order to more clearly illustrate the embodiments of the present invention or the technical solutions in the prior art, the drawings used in the description of the embodiments or the prior art will be briefly described below. It should be apparent that the drawings in the following description are merely exemplary, and that other embodiments can be derived from the drawings provided by those of ordinary skill in the art without inventive effort.
The structure, ratio, size and the like shown in the present specification are only used for matching with the content disclosed in the specification, so as to be known and read by people familiar with the technology, and are not used for limiting the limit conditions which can be implemented by the present invention, so that the present invention has no technical essential significance, and any structure modification, ratio relationship change or size adjustment should still fall within the range which can be covered by the technical content disclosed by the present invention without affecting the efficacy and the achievable purpose of the present invention.
FIG. 1 is a schematic view of the relative positions of a cross member and side plates of a parking apparatus;
fig. 2 is a schematic structural diagram of an embodiment of the present invention;
fig. 3 is a schematic structural diagram of a welding rack in an embodiment of the present invention;
FIG. 4 is a schematic structural diagram of a push plate in an embodiment of the present invention;
fig. 5 is a state diagram of the swing arm in the embodiment of the present invention;
FIG. 6 is a diagram illustrating the swing arm falling state in the embodiment of the present invention;
in the figure: 100. a cross beam 200, a side plate;
1. welding frame, 2, feed roll, 3, vertical support, 4, material pushing box, 5, panel hold the case, 6, first cylinder, 7, layer board, 8, second cylinder, 9, push pedal, 901, bead, 902, magnet, 10, third cylinder, 11, positioning roller, 12, fourth cylinder, 13, sliding roller, 14, linking arm, 15, fifth cylinder, 16, clamp plate, 17, material roller frame, 1701, breach, 18, conveying frame, 1801, conveying beam, 19, swing arm, 20, first sprocket, 21, second sprocket, 22, conveying chain, 23, elevating system, 24, engaging lug, 25, motor, 26, first drive sprocket, 27, second drive sprocket, 28, first drive chain, 29, third drive sprocket, 30, fourth drive sprocket, 31, second drive chain, 32, transmission shaft.
Detailed Description
The present invention is described in terms of specific embodiments, and other advantages and benefits of the present invention will become apparent to those skilled in the art from the following disclosure. Based on the embodiments in the present invention, all other embodiments obtained by a person skilled in the art without creative work belong to the protection scope of the present invention.
In the present specification, the terms "front", "rear", "left", "right", "inner", "outer" and "middle" are used for convenience of description, and are not intended to limit the scope of the present invention, and changes or adjustments of the relative relationship thereof may be made without substantial technical changes.
As shown in figures 2 and 3 together, the welding production line for the cross beam and the side plate of the parking equipment comprises a welding rack 1, wherein two ends of the welding rack 1 are respectively provided with a material roller rack 17, one side of the material roller rack 17 is provided with a conveying rack, the conveying direction of the material roller rack 17 is vertical to the conveying direction of the conveying rack, a plurality of feeding rollers 2 are rotatably arranged on the welding rack 1 and the material roller rack 17, the feeding rollers 2 are generally connected with a chain wheel transmission mechanism driven by a motor and used for conveying the cross beam downstream, a web plate of the cross beam is parallel to the conveying plane of the feeding rollers 2 during conveying, one side of the welding rack 1 is provided with a vertical support 3, a material pushing box 4 is vertically and slidably arranged on the vertical support 3, a plate accommodating box 5 is fixedly arranged below the material pushing box 4, the plate accommodating box 5 is communicated with the material pushing box 4, the bottom of the plate accommodating box 5 is provided with a supporting plate 7 driven by a first air cylinder 6, the cylinder body of the first cylinder 6 is fixedly arranged at the bottom of the plate containing box 5, the piston rod of the first cylinder 6 is connected with the supporting plate 7, the supporting plate 7 is vertically and slidably arranged in the plate containing box 5, a plurality of side plates can be simultaneously and horizontally arranged in the plate containing box 5, namely, the side plates are horizontally stacked on the supporting plate 7, when the side plates need to be provided, the supporting plate 7 supports the side plates to move upwards, the push plate 9 driven by the second cylinder 8 is transversely and slidably arranged in the material pushing box 4, the cylinder body of the second cylinder 8 is fixedly arranged on the material pushing box 4, the piston rod of the second cylinder 8 is connected with the push plate 9, the sliding direction of the push plate 9 is vertical to the sliding direction of the supporting plate 7, after the side plate at the uppermost layer touches the push plate 9 at the initial state, the first cylinder 6 stops moving and does not move upwards, the second cylinder 8 starts to move, and the piston rod of the second cylinder 8 extends out, the push plate 9 is driven to push the uppermost side plate to a welding position on the cross beam, after the welding of the side plate and the cross beam is finished, a piston rod of the second cylinder 8 retracts, the material pushing box 4 is connected with the third cylinder 10, a cylinder body of the third cylinder 10 is fixedly installed on the vertical support 3, a piston rod of the third cylinder 10 is hinged and installed on the material pushing box 4, the material pushing box 4 descends and ascends along with the extension and retraction of the piston rod of the third cylinder 10, the butt joint of the cross beam and the side plate with different specifications is further met, a welding device (not shown in the figure) is arranged at a position, corresponding to the push plate 9, on the welding rack 1, the welding device is welded by using a manual welding robot or welding robot, technical personnel in the field need to set by themselves according to needs, after the butt joint is finished, the welding is carried out, and the combination of the side plate and the cross beam is realized.
As shown in fig. 4, one end of the pushing plate 9 is provided with a protruding rib 901 for pushing and blocking the side plate, and the protruding height of the protruding rib 901 is generally smaller than or equal to the thickness of the side plate, so as to ensure that the pushing plate 9 pushes one side plate at a time. In order to guarantee that the side plate can not drop in the pushing process, the magnet 902 used for adsorbing the side plate is embedded on the push plate 9, the magnet 902 adsorbs the side plate and then is pushed to the beam by the push plate 9, the push plate 9 retracts after welding, so that the magnet 902 is separated from the side plate, and the push plate 9 can continuously adsorb the next side plate.
As shown in fig. 2, 5 and 6, one side of the welding machine frame 1 is provided with a positioning roller 11 for limiting the degree of freedom of the beam horizontally perpendicular to the conveying direction, the positioning roller 11 is used for abutting against one wing plate of the beam to play a role in guiding and positioning, the other side of the welding machine frame 1 is provided with a sliding roller 13, the sliding roller 13 is arranged in parallel with the positioning roller 11, the sliding direction of the sliding roller 13 is horizontally perpendicular to the conveying direction of the feed roller 2, the sliding roller 13 is connected with a fourth cylinder 12, the cylinder body of the fourth cylinder 12 is fixed on the welding machine frame 1, the piston rod of the fourth cylinder 12 is connected with the sliding roller 13, under the action of the fourth cylinder 12, the sliding roller 13 abuts against the other wing plate of the beam to clamp the beam, and within the stroke range of the fourth cylinder 12, clamping of beams with different specifications can be met.
The vertical support 3 is fixedly provided with a connecting arm 14, the connecting arm 14 is provided with a pressing plate 16 which is driven by a fifth cylinder 15 and used for pressing the beam, a cylinder body of the fifth cylinder 15 is fixedly arranged on the connecting arm 14, and a piston rod of the fifth cylinder 15 is connected with the pressing plate 16 and used for pressing the beam on the feed roller 2 so as to ensure that the beam is kept stable in the welding process.
At least two conveying beams 1801 arranged in parallel are arranged on the conveying rack 18, a swing arm 19 is rotatably mounted at the head end of each conveying beam 1801 through a hinge shaft, a first chain wheel 20 connected with a power device is rotatably mounted at the end part of the swing arm 19, a second chain wheel 21 is rotatably mounted at the tail end of each conveying beam 1801, a conveying chain 22 is encircled between the first chain wheel 20 and the second chain wheel 21, a notch 1701 is arranged on one side of the conveying rack 18 on the material roller rack 17 and corresponds to the position of the swing arm 19, the swing arm 19 extends into the notch 1701 and is positioned between two adjacent material conveying rollers 2 and can swing up and down without interference, the swing arm 19 is connected with a lifting mechanism 23, as shown in figures 2 and 3, when a cross beam needs to be transferred from the conveying rack 18 to the material roller rack 17 or from the material roller rack 17 to the conveying rack 18, the lifting mechanism 23 lifts the swing arm 19, the cross beam can reach the conveying position of the material conveying rollers 2 through the swing arm 19 by the conveying chain 22, then elevating system 23 drives swing arm 19 whereabouts, places the crossbeam on feed roll 2, perhaps lifts the crossbeam on the feed roll 2 through swing arm 19, leaves feed roll 2, carries away from feed roll 2 by conveying chain 22, has avoided the crossbeam to drag the line on feed roll 2, can not rub and harm feed roll 2.
The lifting mechanism 23 comprises a sixth air cylinder, the cylinder body of the sixth air cylinder is hinged and installed at a fixed position, the fixed position can be on a foundation, can also be on the conveying rack 18, and can also be on the material roller rack 17, the lifting mechanism can be selected by a person skilled in the art according to needs, the fixing position is not limited, the swing arm 19 is hinged and installed with a connecting lug 24, the piston rod of the sixth air cylinder is hinged with the connecting lug 24, the connecting lug 24 is a common connecting piece used in pneumatic elements and belongs to a standard part, and the lifting mechanism can be selected by the person skilled in the art according to needs. Of course, the lifting mechanism 23 may also be selected from other structures such as a hydraulic cylinder or a telescopic link, and those skilled in the art may select and use the lifting mechanism according to the needs, which will not be described herein.
The articulated shafts of two adjacent delivery beams 1801 are connected through a transmission shaft 32, and the transmission shaft 32 is a rigid shaft, so that the articulated shafts on the delivery beams 1801 rotate synchronously.
The power device comprises a motor 25 in transmission connection with a transmission shaft 32, the motor 25 is usually fixedly installed on the conveyor frame 18, the motor 25 and the transmission shaft 32 can be in chain transmission connection or belt transmission connection or gear transmission connection, etc., the transmission shaft 32 is in transmission connection with the first chain wheel 20, the transmission shaft 32 is usually in transmission connection with the first chain wheel 20 by chain transmission, specifically, the motor 25 is provided with a first transmission chain wheel 26, the transmission shaft 32 is provided with a second transmission chain wheel 27 and a third transmission chain wheel 29, the second transmission chain wheel 27 and the third transmission chain wheel 29 are both fixedly installed at one end of the transmission shaft 32, or the second transmission chain wheel 27 and the third transmission chain wheel 29 can be provided as an integral double-row chain wheel, the first chain wheel 20 is fixedly connected with a fourth transmission chain wheel 30, and a first transmission chain 28 is arranged between the first transmission chain wheel 26 and the second transmission chain wheel 27, and a second transmission chain 31 is arranged between the third transmission chain wheel 29 and the fourth transmission chain wheel 30, so that the power transmission of the first chain wheel 20 can be ensured, the swing arm 19 can swing freely without influencing the power transmission, the structure is ingenious, and the use is flexible and reliable.
Because the articulated shaft is rigidly connected through the transmission shaft 32, the conveying chain 22 only needs one group of motors 25 for transmission, thereby simplifying the structure, ensuring the synchronization of the conveying chain 22, reducing the use of power and reducing the cost.
During the use, according to the specification of crossbeam, adjust the piston rod extension length of third cylinder 10 for the width looks adaptation of push pedal 9 propelling movement position and crossbeam pterygoid lamina, the piston rod extension length of adjustment fifth cylinder 15 makes the clamp plate 16 compress tightly the crossbeam on the feed roll 2 when pushing down, sets up each cylinder in initial condition, and at this moment, the piston rod of first cylinder 6, second cylinder 8, third cylinder 10, fourth cylinder 12 and fifth cylinder 15 all is in the withdrawal position. When feeding, the lifting mechanism 23 lifts the swing arm 19, the cross beam can reach the conveying position of the feeding roller 2 through the conveying chain 22 via the swing arm 19, then the lifting mechanism 23 drives the swing arm 19 to fall down, the cross beam is placed on the feeding roller 2 to complete feeding of the cross beam, the cross beam is conveyed from the feeding roller 2 to the downstream, when the specified position is reached, the piston rod of the fourth cylinder 12 extends out, the slide roller 13 and the positioning roller 11 clamp the cross beam tightly, the fifth cylinder 15 drives the pressing plate 16 to press down, the cross beam is pressed on the feeding roller 2 to complete positioning of the cross beam, the third cylinder 10 drives the material pushing box 4 to move down, then the first cylinder 6 drives the supporting plate 7 to move up, after the side plate on the uppermost layer touches the pushing plate 9 in the initial state, the first cylinder 6 stops moving and does not move up, the second cylinder 8 starts to move, the piston rod of the second cylinder 8 extends out to drive the pushing plate 9 to push the uppermost side plate to the welding position on the cross beam, realize butt joint curb plate and crossbeam, then implement the welding by manual work or robot, after curb plate and crossbeam welding, each cylinder resets, prepares the butt joint of next curb plate, and feed roll 2 carries the crossbeam that the welding was accomplished to the low reaches position, and the elevating system 23 that is located the low reaches lifts swing arm 19, and swing arm 19 lifts the crossbeam, leaves feed roll 2, carries away from feed roll 2 by conveying chain 22, accomplishes the crossbeam and unloads.
The utility model discloses can set up corresponding interfacing apparatus according to the quantity and the position of required welding curb plate on the crossbeam, welding frame 1 that these interfacing apparatus can share further improves the butt joint efficiency of curb plate and crossbeam.
To sum up, the embodiment of the utility model provides a parking equipment crossbeam and curb plate welding production line needn't rely on the manual work to fix a position crossbeam and curb plate, have realized the butt joint of crossbeam and curb plate, labour saving and time saving has improved the machining efficiency of crossbeam greatly.
Although the invention has been described in detail with respect to the general description and the specific embodiments, it will be apparent to those skilled in the art that modifications and improvements can be made based on the invention. Therefore, such modifications and improvements are intended to be within the scope of the invention as claimed.