CN110253304B - An elevator door panel rolling production line - Google Patents
An elevator door panel rolling production line Download PDFInfo
- Publication number
- CN110253304B CN110253304B CN201910491759.7A CN201910491759A CN110253304B CN 110253304 B CN110253304 B CN 110253304B CN 201910491759 A CN201910491759 A CN 201910491759A CN 110253304 B CN110253304 B CN 110253304B
- Authority
- CN
- China
- Prior art keywords
- roller
- cylinder
- line
- frame
- unpowered
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P23/00—Machines or arrangements of machines for performing specified combinations of different metal-working operations not covered by a single other subclass
- B23P23/06—Metal-working plant comprising a number of associated machines or apparatus
Landscapes
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Automobile Manufacture Line, Endless Track Vehicle, Trailer (AREA)
- Gates (AREA)
Abstract
本发明涉及一种电梯门壁板滚压生产线,属于电梯制造技术领域,通过四段无动力滚筒线、一台自动滚压机组成一条滚压生产线,通过在前二段无动力滚筒线上进行打胶、加强筋的粘贴,中间通过滚压机对加强肋进行自动滚压压紧,在后二段无动力滚筒线上进行厅门及加强筋的无铆连接、轿门及加强筋的拉铆连接,轿壁及加强筋的拉铆连接,实现了电梯门壁板滚压等整个流程的流水线的生产,提高了生产效率,降低了人力成本,同时避免了工艺与工艺之间不连贯而需人工搬运产品导致零件表面损伤。同时,本发明在整个工艺的尾端增设万向滚珠台,通过万向滚珠台实现对经过滚压加工后的电梯门壁板转向,使产品进入下一道生产工艺,进一步避免人工搬运电梯门壁板。
The invention relates to a rolling production line for elevator door wall panels, which belongs to the technical field of elevator manufacturing. A rolling production line is composed of four sections of unpowered drum lines and an automatic rolling machine. Glue, sticking of reinforcing ribs, automatic rolling and pressing of reinforcing ribs by rolling machine in the middle, rivet-free connection of hall door and reinforcing ribs, pulling of car doors and reinforcing ribs on the last two unpowered roller lines The riveted connection, the pull riveted connection of the car wall and the reinforcing ribs, realizes the production of the whole process of the elevator door wall plate rolling, etc., improves the production efficiency, reduces the labor cost, and avoids the incoherence between the process and the process. Manual handling of the product results in damage to the surface of the parts. At the same time, the invention adds a universal ball table at the end of the whole process, and realizes the turning of the elevator door panel after rolling processing through the universal ball table, so that the product enters the next production process, and further avoids manual handling of the elevator door wall. plate.
Description
技术领域technical field
本发明属于电梯制造技术领域,具体地说,涉及一种电梯门壁板滚压生产线。The invention belongs to the technical field of elevator manufacturing, in particular to a rolling production line for elevator door wall panels.
背景技术Background technique
目前,在电梯门壁板的生产过程中,电梯门壁板的门壁板打胶、加强筋的粘贴等都是人工分段进行,没有把工艺形成一个系统的生产线方式,而是人工把上环节的工艺完成后送往下一道工序,在中转上浪费时间及还容易把零件表面弄伤。并且,加强肋滚压是通人工来滚压,人工滚压不好控制滚压的速度及力度,这样容易造成压胶不平,或胶里夹杂空气,从而使加强肋与壁板连接不牢固,粘连位置不正确,造成后序工艺的配合不上,通过这种工艺来生产会造成工作强度高,而且速度慢,不良率高,不能满足现有的生产效率。At present, in the production process of elevator door panels, the door panels of elevator door panels are glued and the reinforcing ribs are pasted manually. After the process of the link is completed, it is sent to the next process, which wastes time in transit and easily damages the surface of the parts. In addition, the reinforcing rib rolling is manually rolled, and the manual rolling cannot control the speed and strength of the rolling, which is easy to cause uneven pressing, or air is mixed in the glue, so that the connection between the reinforcing rib and the wall is not firm. The adhesion position is incorrect, resulting in the failure of the subsequent process. Production through this process will result in high work intensity, slow speed, and high defect rate, which cannot meet the existing production efficiency.
发明内容SUMMARY OF THE INVENTION
为了克服背景技术中存在的问题,本发明提供了一种电梯门壁板滚压生产线,通过利用四段无动力滚筒线配合一台自动滚压机组成一条电梯门壁板滚压生产线,通过在前二段无动力滚筒线上进行打胶、加强筋的粘贴,中间通过滚压机对加强肋进行自动滚压压紧,在后二段无动力滚筒线上进行厅门及加强筋的无铆连接、轿门及加强筋的拉铆连接,轿壁及加强筋的拉铆连接,整个工艺不需要人工搬运,同时实现了加强肋的自动滚压压紧,实现了电梯门壁板滚压等整个流程的流水线的生产,提高了生产效率,降低了人力成本,同时避免了工艺与工艺之间不连贯而需人工搬运产品导致零件表面损伤。In order to overcome the problems existing in the background technology, the present invention provides an elevator door panel rolling production line, which is composed of an elevator door panel rolling production line by using four sections of unpowered roller lines and an automatic rolling machine to form an elevator door panel rolling production line. The first two sections of the unpowered drum line are glued and the reinforcing ribs are pasted. In the middle, the reinforcing ribs are automatically rolled and compacted by the rolling machine. Connection, pull riveting connection of car door and reinforcing rib, pull riveting connection of car wall and reinforcing rib, the whole process does not require manual handling, and at the same time realizes automatic rolling and pressing of reinforcing ribs, and realizes rolling of elevator door wall panels, etc. The production line of the whole process improves production efficiency, reduces labor costs, and avoids the inconsistency between processes and the need to manually transport products to cause surface damage of parts.
为实现上述目的,本发明是通过如下技术方案实现的:To achieve the above object, the present invention is achieved through the following technical solutions:
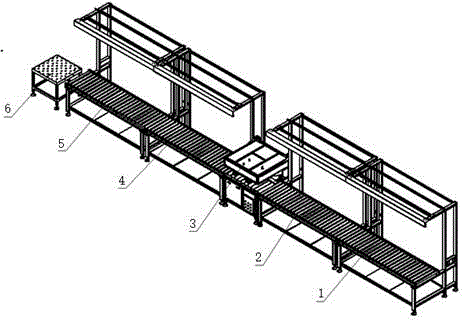
所述的电梯门壁板滚压生产线包括无动力滚筒线Ⅰ1、无动力滚筒线Ⅱ2、滚压机3、无动力滚筒线Ⅲ4、无动力滚筒线Ⅳ5,所述的无动力滚筒线Ⅰ1与无动力滚筒线Ⅱ2并排安装,无动力滚筒线Ⅲ4与无动力滚筒线Ⅳ5并排安装,动力滚筒线Ⅱ2与无动力滚筒线Ⅲ4之间安装有滚压机3。The elevator door panel rolling production line includes unpowered roller line I1, unpowered roller line II2,
进一步,所述的无动力滚筒线Ⅰ1、无动力滚筒线Ⅱ2、无动力滚筒线Ⅲ4、无动力滚筒线Ⅳ5的结构相同,均包括滚筒机架7、滚筒支架8、无动力滚筒9、日光灯罩10、挂勾滑架11、气管12,所述的滚筒机架7的前侧顶部安装有滚筒支架8,滚筒支架8上安装有无动力滚筒9,滚筒机架7的顶部前侧安装有日光灯罩10,滚筒机架7的顶部安装有挂勾滑架11、气管12。Further, the unpowered drum line I1, the unpowered drum line II2, the unpowered drum line III4, and the unpowered drum line IV5 have the same structure, including a drum frame 7, a
进一步,所述的滚筒机架7的下部设置有置物层板13。Further, the lower part of the drum frame 7 is provided with a
进一步,所述的滚筒机架7的底部安装有用于支撑整个滚筒机架7以及调整滚筒机架7高度的调节脚杯14。Further, the bottom of the drum frame 7 is provided with an adjusting
进一步,所述的滚压机3包括机架15、滚压装置16、动力滚筒装置17,所述的动力滚筒装置17安装在机架15上,动力滚筒装置17上方的机架15上安装有与其正对的滚压装置16,机架15的底部设置有调节脚杯14。Further, the
进一步,所述的动力滚筒装置17包括滚筒安装板18、动力滚筒19、减速电机20、链轮传动机构21、盖板23,机架15上平行安装有两块滚筒安装板18,动力滚筒19通过轴承整齐排列安装在两块滚筒安装板18上,相邻两个动力滚筒19通过链轮机构连接,其中一个动力滚筒19通过链轮传动机构21与安装在机架15上的减速电机20连接,机架15上安装有用于防护链轮传动机构21的盖板23。Further, the
进一步,所述的机架15上安装有用于张紧链轮传动机构21传动链条的张紧机构22,张紧机构22包括张紧座24、张紧轮轴25、张紧链轮26,所述的张紧座24固定安装在机架15上,张紧座24上开设有一个条形安装槽,张紧轮轴25安装在条形安装槽内,张紧链轮26通过轴承安装在张紧轮轴25上,张紧链轮26与链轮传动机构21的传动链轮啮合。Further, the
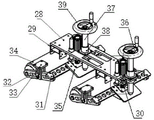
所述的滚压装置16包括调节固定板28、安装座29、气动下压装置30、过渡连接板31、滚筒连杆32、铰链座33、滚压滚筒34、上下调节压板35;所述的调节固定板28通过安装座29固定安装在机架15上,上下调节压板35固定连接在过渡连接板31上,过渡连接板31的两侧分别通过固定螺丝安装有一块滚筒连杆32,滚筒连杆32的中部通过销轴与安装在机架15上的铰链座33铰接,滚压滚筒34通过轴承安装在两块滚筒连杆32的悬端,机架15上安装有两个能够与滚压滚筒34一一对应且实现滚压滚筒34下压的气动下压装置30。The
进一步,所述的气动下压装置30包括薄壁气缸40、气缸连接头41、气缸连接座42、导杆安装板43、垫块44、压轮固定座45、压轮销轴46、压轮47、导套48、导杆49,所述的薄壁气缸40固定安装在调节固定板28顶部,薄壁气缸40的活塞杆上安装有气缸连接头41,导杆安装板43通过气缸连接座42安装在气缸连接头41的底部,导杆安装板43上设置有导杆49,导杆49穿过固定安装在调节固定板28上的导套48,导杆安装板43的底部安装有垫块44,压轮固定座45安装在垫块44上,压轮47通过压轮销轴46安装在压轮固定座45上。Further, the pneumatic
进一步,滚压装置16还包括上下调节机构36,上下调节机构36包括T形丝杆37、T形螺母38、手轮39,所述的T形螺母38贯穿安装在调节固定板28上,T形丝杆37安装在T形螺母38内,T形丝杆37的上端安装有手轮39。Further, the
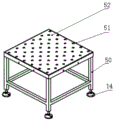
进一步,所述的无动力滚筒线Ⅳ5的后侧设置有万向滚珠台6,万向滚珠台6包括支架50、万向滚珠轮51、封板52,所述的支架50底部安装有调节脚杯14,支架50的顶部为一平整台面,台面上均匀的开设凹槽,凹槽内放置万向滚珠轮51,封板52上开设有与支架50台面上数量一致且一一对应的通孔,封板52压盖在万向滚珠轮51上且万向滚珠轮51的上部从通孔中穿出,封板52四周固定在支架50上。Further, a universal ball table 6 is arranged on the rear side of the described unpowered roller line IV5, and the universal ball table 6 includes a
本发明的有益效果:Beneficial effects of the present invention:
通过利用四段无动力滚筒线配合一台自动滚压机组成一条电梯门壁板滚压生产线,通过在前二段无动力滚筒线上进行打胶、加强筋的粘贴,中间通过滚压机对加强肋进行自动滚压压紧,在后二段无动力滚筒线上进行厅门及加强筋的无铆连接、轿门及加强筋的拉铆连接,轿壁及加强筋的拉铆连接,整个工艺不需要人工搬运,同时实现了加强肋的自动滚压压紧,实现了电梯门壁板滚压等整个流程的流水线的生产,提高了生产效率,降低了人力成本,同时避免了工艺与工艺之间不连贯而需人工搬运产品导致零件表面损伤。同时,本发明在整个工艺的尾端增设万向滚珠台,通过万向滚珠台实现对经过滚压加工后的电梯门壁板转向,使产品进入下一道生产工艺,进一步避免了人工搬运电梯门壁板。An elevator door panel rolling production line is formed by using four sections of unpowered roller lines and an automatic rolling machine. By applying glue and sticking reinforcing ribs on the first two sections of unpowered roller lines, the rolling machine is used in the middle. The reinforcing rib is automatically rolled and pressed, and the riveted connection of the hall door and the reinforcing rib, the riveted connection of the car door and the reinforcing rib, the riveted connection of the car wall and the reinforcing rib, and the riveted connection of the car wall and the reinforcing rib are carried out on the unpowered roller line of the last two sections. The process does not require manual handling, and at the same time, the automatic rolling and pressing of the reinforcing ribs is realized, and the production line of the whole process of rolling of the elevator door wall plate is realized, which improves the production efficiency, reduces the labor cost, and avoids the process and technology. Inconsistencies between parts require manual handling of the product resulting in surface damage to the part. At the same time, the invention adds a universal ball table at the end of the whole process, and realizes the turning of the elevator door panel after rolling processing through the universal ball table, so that the product enters the next production process, and further avoids manual handling of the elevator door. siding.
附图说明Description of drawings
图1为本发明的结构示意图;Fig. 1 is the structural representation of the present invention;
图2为本发明无动力滚筒线Ⅰ、无动力滚筒线Ⅱ、无动力滚筒线Ⅲ、无动力滚筒线Ⅳ的结构示意图;Figure 2 is a schematic structural diagram of the unpowered drum line I, the unpowered drum line II, the unpowered drum line III, and the unpowered drum line IV of the present invention;
图3为本发明滚压机的结构示意图;Fig. 3 is the structural representation of the rolling machine of the present invention;
图4为本发明滚压机的左视图;Fig. 4 is the left side view of the rolling machine of the present invention;
图5为本发明动力滚筒装置的结构示意图;5 is a schematic structural diagram of a power roller device of the present invention;
图6为本发明动力滚筒装置的左视图;Fig. 6 is the left side view of the power roller device of the present invention;
图7为本发明滚压装置的结构示意图;Fig. 7 is the structural representation of the rolling device of the present invention;
图8为本发明下压装置的结构示意图;8 is a schematic structural diagram of the pressing device of the present invention;
图9为本发明万向滚珠台的结构示意图;9 is a schematic structural diagram of a universal ball table of the present invention;
图10为本发明张紧机构的结构示意图。FIG. 10 is a schematic structural diagram of the tensioning mechanism of the present invention.
图中,1-无动力滚筒线Ⅰ、2-无动力滚筒线Ⅱ、3-滚压机、4-无动力滚筒线Ⅲ、5-无动力滚筒线Ⅳ、6-万向滚珠台、7-滚筒机架、8-滚筒支架、9-无动力滚筒、10-日光灯罩、11-挂勾滑架、12-气管、13-置物层板、14-调节脚杯、15-机架、16-滚压装置、17-动力滚筒装置、18-滚筒安装板、19-动力滚筒、20-减速电机、21-链轮传动机构、22-张紧机构、23-盖板、24-张紧座、25-张紧轮轴、26-张紧链轮、28-调节固定板、29-安装座、30-下压装置、31-过渡连接板、32-滚筒连杆、33-铰链座、34-滚压滚筒、35-上下调节压板、36-上下调节机构、37- T形丝杆、38-T形螺母、39-手轮、40-薄壁气缸、41-气缸连接头、42-气缸连接座、43-导杆安装板、44-垫块、45-压轮固定座、46-压轮销轴、47-压轮、48-导套、49-导杆、50-支架、51-万向滚珠轮、52-封板。In the figure, 1-unpowered roller line I, 2-unpowered roller line II, 3-roller, 4-unpowered roller line III, 5-unpowered roller line IV, 6-universal ball table, 7- Roller rack, 8-roller bracket, 9-unpowered roller, 10-fluorescent lamp shade, 11-hook carriage, 12-air pipe, 13-shelf, 14-adjustable foot cup, 15-rack, 16- Rolling device, 17-power roller device, 18-roller mounting plate, 19-power roller, 20-deceleration motor, 21-sprocket transmission mechanism, 22-tension mechanism, 23-cover plate, 24-tension seat, 25- Tensioning wheel shaft, 26- Tensioning sprocket, 28- Adjusting fixed plate, 29- Mounting seat, 30- Pressing device, 31- Transition connecting plate, 32- Roller connecting rod, 33- Hinge seat, 34- Roller Pressure roller, 35-up and down adjustment platen, 36-up and down adjustment mechanism, 37-T-shaped screw rod, 38-T-shaped nut, 39-handwheel, 40-thin-wall cylinder, 41-cylinder connection head, 42-cylinder connection seat , 43- Guide rod mounting plate, 44- Spacer block, 45- Pressure wheel fixing seat, 46- Pressure wheel pin, 47- Pressure wheel, 48- Guide sleeve, 49- Guide rod, 50- Bracket, 51- Universal direction Ball wheel, 52-sealing plate.
具体实施方式Detailed ways
下面将结合本发明实施例和附图,对本发明实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本发明一部分实施例,而不是全部的实施例。基于本发明中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本发明保护的范围。The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the embodiments of the present invention and the accompanying drawings. Obviously, the described embodiments are only a part of the embodiments of the present invention, rather than all the embodiments. Based on the embodiments of the present invention, all other embodiments obtained by those of ordinary skill in the art without creative efforts shall fall within the protection scope of the present invention.
如图1所示,所述的电梯门壁板滚压生产线包括无动力滚筒线Ⅰ1、无动力滚筒线Ⅱ2、滚压机3、无动力滚筒线Ⅲ4、无动力滚筒线Ⅳ5,所述的无动力滚筒线Ⅰ1与无动力滚筒线Ⅱ2并排安装,无动力滚筒线Ⅲ4与无动力滚筒线Ⅳ5并排安装,动力滚筒线Ⅱ2与无动力滚筒线Ⅲ4之间安装有滚压机3。As shown in Fig. 1, the elevator door panel rolling production line includes unpowered roller line I1, unpowered roller line II2, rolling
如图2所示,所述的无动力滚筒线Ⅰ1、无动力滚筒线Ⅱ2、无动力滚筒线Ⅲ4、无动力滚筒线Ⅳ5的结构相同,均包括滚筒机架7、滚筒支架8、无动力滚筒9、日光灯罩10、挂勾滑架11、气管12,所述的滚筒机架7的前侧顶部安装有滚筒支架8,滚筒支架8上安装有无动力滚筒9,滚筒机架7的顶部前侧安装有日光灯罩10,滚筒机架7的顶部安装有挂勾滑架11、气管12。通过将将电梯门壁板放置在无动力滚筒线Ⅰ1的无动力滚筒9上,然后人为对电梯门壁板进行打胶,然后人为即可通过无动力滚筒9轻松快速的推入无动力滚筒线Ⅱ2的无动力滚筒9上,人工将加强筋粘贴在电梯门壁板上。加强筋粘贴完毕后,工作人员将电梯门壁板推入到滚压机3对加强筋进行滚压。其中还设置挂勾滑架11来放置工具,可以整齐有顺的把工具挂在挂勾滑架11上,根据生产的需要取用工具;通过设置的气管12可以与气压设备连通,在生产过程中可以通过气管将电梯门壁板上的灰尘清理干净。通过设置有日光灯罩10,将日光灯安装在日光灯罩10内,可以为工作提供照明。As shown in Figure 2, the unpowered drum line I1, the unpowered drum line II2, the unpowered drum line III4, and the unpowered drum line IV5 have the same structure, including a drum frame 7, a
在本发明中,作为优选,所述的滚筒机架7的下部设置有置物层板13。置物层板13用来放置装配上的零件及辅件,保证零件及辅件的堆放有序。In the present invention, preferably, the lower part of the drum frame 7 is provided with a
在本发明中,作为优选,所述的滚筒机架7的底部安装有用于支撑整个滚筒机架7以及调整滚筒机架7高度的调节脚杯14。以保证无动力滚筒线Ⅰ1、无动力滚筒线Ⅱ2、无动力滚筒线Ⅲ4、无动力滚筒线Ⅳ5的无动力滚筒9在同一水平线上,便于电梯门壁板的传送。In the present invention, preferably, the bottom of the drum frame 7 is provided with an adjusting
如图3、4所示,所述的滚压机3包括机架15、滚压装置16、动力滚筒装置17,所述的动力滚筒装置17安装在机架15上,动力滚筒装置17上方的机架15上安装有与其正对的滚压装置16,机架15的底部设置有调节脚杯14。As shown in FIGS. 3 and 4 , the rolling
如图5、6所示,所述的动力滚筒装置17包括滚筒安装板18、动力滚筒19、减速电机20、链轮传动机构21、盖板23,机架15上平行安装有两块滚筒安装板18,动力滚筒19通过轴承整齐排列安装在两块滚筒安装板18上,相邻两个动力滚筒19通过链轮机构连接,其中一个动力滚筒19通过链轮传动机构21与安装在机架15上的减速电机20连接,机架15上安装有用于防护链轮传动机构21的盖板23。减速电机20通过链轮传动机构21带动与其连接的动力滚筒19转动,该动力滚筒19通过过链轮机构带动其他动力滚筒19转动,在本发明中,作为优选,如图10所示,所述的机架15上安装有用于张紧链轮传动机构21传动链条的张紧机构22,张紧机构22包括张紧座24、张紧轮轴25、张紧链轮26,所述的张紧座24固定安装在机架15上,张紧座24上开设有一个条形安装槽,张紧轮轴25安装在条形安装槽内,张紧链轮26通过轴承安装在张紧轮轴25上,张紧链轮26与链轮传动机构21的传动链轮啮合。通过调整张紧轮轴25在张紧座24上条形安装槽内的位置,从而调整张紧链轮26的位置,通过张紧链轮26实现链轮传动机构21的传动链张紧,保证链轮传动机构21能够稳定工作。当电梯门壁板推入到动力滚筒19上时,在减速电机20的驱动下,通过转动的动力滚筒19向前输送电梯门壁板。As shown in FIGS. 5 and 6 , the
如图7所示,所述的滚压装置16包括调节固定板28、安装座29、气动下压装置30、过渡连接板31、滚筒连杆32、铰链座33、滚压滚筒34、上下调节压板35;所述的调节固定板28通过安装座29固定安装在机架15上,上下调节压板35固定连接在过渡连接板31上,过渡连接板31的两侧分别通过固定螺丝安装有一块滚筒连杆32,滚筒连杆32的中部通过销轴与安装在机架15上的铰链座33铰接,滚压滚筒34通过轴承安装在两块滚筒连杆32的悬端,机架15上安装有两个能够与滚压滚筒34一一对应且实现滚压滚筒34下压的气动下压装置30。所述的气动下压装置30包括薄壁气缸40、气缸连接头41、气缸连接座42、导杆安装板43、垫块44、压轮固定座45、压轮销轴46、压轮47、导套48、导杆49,所述的薄壁气缸40固定安装在调节固定板28顶部,薄壁气缸40的活塞杆上安装有气缸连接头41,导杆安装板43通过气缸连接座42安装在气缸连接头41的底部,导杆安装板43上设置有导杆49,导杆49穿过固定安装在调节固定板28上的导套48,导杆安装板43的底部安装有垫块44,压轮固定座45安装在垫块44上,压轮47通过压轮销轴46安装在压轮固定座45上。当电梯门壁板在动力滚筒19传送作用下,进入到滚压装置16时,滚压装置16的滚压滚筒34会被向上抬起,使其压在电梯门壁板的表面上,通过滚压滚筒34对加强筋进行滚压对电梯门壁板加强筋施加压力,达到电梯门壁板与加强筋通过胶水达到贴合的效果;本发明通过两个滚压装置16对电梯门壁板的加强筋进行滚压,可以保证加强筋的贴合效果。在此过程中,滚压滚筒34是在自重下对电梯门壁板进行滚压的,当电梯门壁板从电梯门壁板的下方通过时会把滚压滚筒34向上抬起来,薄壁气缸40气动将其活塞杆伸出,推出压轮固定座45,使通过压轮销轴46安装在压轮固定座45上的压轮47下压顶在过渡连接板31上,防止滚压滚筒34发生跳动,保证滚压滚筒34始终具有一定的力度压在电梯门壁板上,使电梯门壁板与加强筋紧密贴合。As shown in FIG. 7 , the rolling
在本发明中,作为优选,滚压装置16还包括上下调节机构36,上下调节机构36包括T形丝杆37、T形螺母38、手轮39,所述的T形螺母38贯穿安装在调节固定板28上,T形丝杆37安装在T形螺母38内,T形丝杆37的上端安装有手轮39。当薄壁气缸40的气压不稳定或其他原因导致滚压滚筒34发生跳动时,可通过手轮39调节T形丝杆37向下运动,使其下端顶住上下调节板35,防止滚压滚筒34跳动,从而保证滚压滚筒34始终具有一定的力度施压在电梯门壁板上,从而保证电梯门壁板与加强筋紧密贴合。In the present invention, preferably, the rolling
贴合加强筋的电梯门壁板在动力滚筒19输送下,进入到无动力滚筒线Ⅲ4与无动力滚筒线Ⅳ5,通过人工实现电梯厅门及加强筋的无铆连接,轿门及加强筋的拉铆连接,轿壁及加强筋的拉铆连接,完成产品该阶段的加工。The elevator door panel fitted with the reinforcing rib is conveyed by the
如图9所示,所述的无动力滚筒线Ⅳ5的后侧设置有万向滚珠台6,万向滚珠台6包括支架50、万向滚珠轮51、封板52,所述的支架50底部安装有调节脚杯14,支架50的顶部为一平整台面,台面上均匀的开设凹槽,凹槽内放置万向滚珠轮51,封板52上开设有与支架50台面上数量一致且一一对应的通孔,封板52压盖在万向滚珠轮51上且万向滚珠轮51的上部从通孔中穿出,封板52四周固定在支架50上。加工完成的产品则通过人工从无动力滚筒线Ⅳ5轻松推到万向滚珠台6上,在万向滚珠轮51的作用下,可通过人工轻松实现电梯的换向,使产品进入下一道工艺。As shown in FIG. 9 , a universal ball table 6 is provided on the rear side of the unpowered roller line IV5. The universal ball table 6 includes a
本发明这个过程无需人工搬运电梯门壁板,通过无动力滚筒线Ⅰ1、无动力滚筒线Ⅲ4、无动力滚筒线Ⅳ5以及万向滚珠台6即可实现电梯门壁板的快速轻松运送以及换向转运。The process of the present invention does not require manual handling of the elevator door panel, and the elevator door panel can be quickly and easily transported and reversed through the unpowered roller line I1, the unpowered roller line III4, the unpowered roller line IV5 and the universal ball table 6 transport.
最后说明的是,以上实施例仅用以说明本发明的技术方案而非限制,尽管通过上述优选实施例已经对本发明进行了详细的描述,但本领域技术人员应当理解,可以在形式上和细节上对其作出各种各样的改变,而不偏离本发明权利要求书所限定的范围。Finally, it should be noted that the above embodiments are only used to illustrate the technical solutions of the present invention and not to limit them. Although the present invention has been described in detail through the above preferred embodiments, those skilled in the art should Various changes can be made thereto without departing from the scope of the invention as defined by the claims.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201910491759.7A CN110253304B (en) | 2019-06-06 | 2019-06-06 | An elevator door panel rolling production line |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201910491759.7A CN110253304B (en) | 2019-06-06 | 2019-06-06 | An elevator door panel rolling production line |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN110253304A CN110253304A (en) | 2019-09-20 |
| CN110253304B true CN110253304B (en) | 2020-12-08 |
Family
ID=67917036
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201910491759.7A Active CN110253304B (en) | 2019-06-06 | 2019-06-06 | An elevator door panel rolling production line |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN110253304B (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110976192A (en) * | 2019-11-22 | 2020-04-10 | 莆田市牧升贸易有限公司 | Elevator door wallboard rolling production line |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH02139145A (en) * | 1988-11-14 | 1990-05-29 | Kawasaki Heavy Ind Ltd | Flanging method for beam of i type |
| CN103832619A (en) * | 2014-03-26 | 2014-06-04 | 朱振西 | Automatic conveying film sticking machine |
| CN203888329U (en) * | 2014-05-16 | 2014-10-22 | 珠海全宝电子科技有限公司 | Efficient heat-conductive adhesive film sticking machine |
| CN204603996U (en) * | 2015-04-15 | 2015-09-02 | 晋江市万益机械制造有限公司 | A kind of modified lines double side polishing machine |
| CN204771569U (en) * | 2014-12-23 | 2015-11-18 | 天津慧霖科技有限公司 | Case and bag hub automation shaping all -in -one of bending |
| CN206264543U (en) * | 2016-10-18 | 2017-06-20 | 蓝思科技股份有限公司 | A kind of automatic heating knurling machine |
| CN207156452U (en) * | 2017-07-15 | 2018-03-30 | 南京禾华塑业有限公司 | A kind of embossing device |
-
2019
- 2019-06-06 CN CN201910491759.7A patent/CN110253304B/en active Active
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH02139145A (en) * | 1988-11-14 | 1990-05-29 | Kawasaki Heavy Ind Ltd | Flanging method for beam of i type |
| CN103832619A (en) * | 2014-03-26 | 2014-06-04 | 朱振西 | Automatic conveying film sticking machine |
| CN203888329U (en) * | 2014-05-16 | 2014-10-22 | 珠海全宝电子科技有限公司 | Efficient heat-conductive adhesive film sticking machine |
| CN204771569U (en) * | 2014-12-23 | 2015-11-18 | 天津慧霖科技有限公司 | Case and bag hub automation shaping all -in -one of bending |
| CN204603996U (en) * | 2015-04-15 | 2015-09-02 | 晋江市万益机械制造有限公司 | A kind of modified lines double side polishing machine |
| CN206264543U (en) * | 2016-10-18 | 2017-06-20 | 蓝思科技股份有限公司 | A kind of automatic heating knurling machine |
| CN207156452U (en) * | 2017-07-15 | 2018-03-30 | 南京禾华塑业有限公司 | A kind of embossing device |
Also Published As
| Publication number | Publication date |
|---|---|
| CN110253304A (en) | 2019-09-20 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN2714297Y (en) | Tire shoulder pad rubber feeding shelf of tire builder | |
| CN108750668A (en) | A kind of door of elevator production line feeding and conveying device | |
| CN119568822A (en) | Automatic winding glue production line for busbar shielding | |
| CN114208603A (en) | A lawn automatic tiling device for improving garden construction efficiency | |
| CN107380936B (en) | Intelligent transfer system applied to weaving workshop | |
| CN204847558U (en) | Automatic rubberizing machine | |
| CN214558413U (en) | A welding production line for longitudinal beam and connecting plate of parking equipment | |
| CN111873090A (en) | A fully automatic plywood blank assembly device | |
| CN207594155U (en) | A kind of feed device of the big frame automatic film applicator of television set | |
| CN214989063U (en) | Automatic core shaft pulling device for threading core | |
| CN110253304A (en) | Elevator door wallboard rolling production line | |
| CN219112797U (en) | Metal plate pressing and riveting device of metal plate machining equipment | |
| CN118888485A (en) | Photovoltaic double-glass module frame removal and tape removal device and method | |
| CN218319287U (en) | A kind of PCBA board feeding equipment | |
| CN208037639U (en) | A kind of steel band storage shelf | |
| CN210549492U (en) | Elevator door wallboard rolling production line | |
| CN212220670U (en) | Gypsum lines tectorial membrane is with preventing guider that inclines | |
| CN212384934U (en) | Fixing device for welding elevator guide rail | |
| CN115159867A (en) | Automatic edge covering equipment for glass transportation and working method thereof | |
| CN220011585U (en) | Intaglio printing press paper feeding device | |
| CN115388076A (en) | Automatic assembly device of compound aluminum plate of high strength | |
| CN109178521B (en) | Labeling device capable of preventing edge from being warped efficiently | |
| CN211970644U (en) | A multilayer conveying equipment for production of novel building wall material | |
| CN211136566U (en) | External trimming workbench device for plate production | |
| CN115009915A (en) | A device for sticking tape |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| PE01 | Entry into force of the registration of the contract for pledge of patent right |
Denomination of invention: A roll forming production line for elevator door panels Granted publication date: 20201208 Pledgee: Bank of Guangzhou Co.,Ltd. Zhongshan branch Pledgor: ZHONGSHAN SANDI CONVEYING EQUIPMENT CO.,LTD. Registration number: Y2025980053340 |
|
| PE01 | Entry into force of the registration of the contract for pledge of patent right |